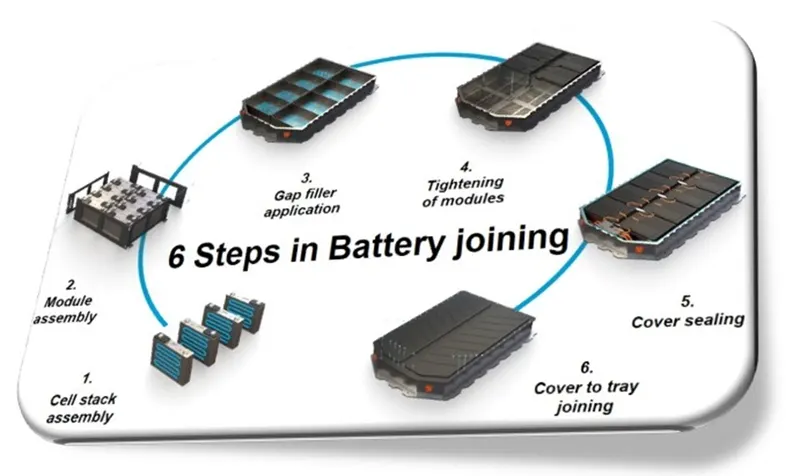
Project 1 Mechanical design of battery pack
From the ANR26650M1-B cell Data Sheet specifications following observations made:-
Assumptions :
Energy ( capacity ) = 18 Kwh
Voltage required to run system = 300 V
From Specification Data
Cell Nominal voltage = 3.3 V
Capacity = 2.5 A
Weight of cell = 76gms
1) Cell in Series = voltage required/Nominal voltage
= 300/3.3
= 90.9
= Aprox. 91 cells
2) Cells in Parallel = Total no. of cells / Cell in series
Total no. of cells = Energy / (Nominal voltage * Capacity)
= 18000/(3.3*2.5)
= 2181.8
= Apprx. 2182 cells
Hence cell in Parallel = 2182/91
= 23.97
= Aprox. 24
Therefore cells are joined in series are 91 and in parallel are 24.
Weight of the Battery pack considering only cell = Total no.cells * Weight of cell
= 2182*76
=165832
= 165.832 Kg
Design Conclusion:-
Cells in Series = 91 cells
Cells in parallel = 24 cells
Total No. of cells in a Battery pack = 2182 cells
Battery pack weight (considering only cells) = 165.832 Kg
Depend upon the design process joining and module packing is considered.
EXPLANATION ON BATTERY PACK ASSEMBLY
Battery
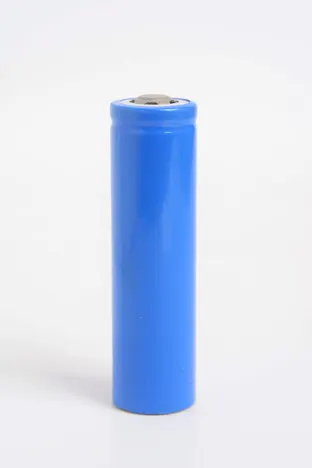
A collection of two or more cells which are connected in series is called A Battery. A battery is an energy source that converts chemical energy to electrical energy. It is otherwise known as Electrochemical Cell. The energy is stored in the form of chemical energy inside a battery. Batteries give us a convenient source of energy for energizing devices without cables and wires. When it is connected to a circuit it produces electrical energy. A battery consists of two terminals – A Positive and Negative Terminal. The positive terminal is called Cathode and the negative terminal is called Anode. They are also called as Electrodes of a Cell. These electrodes will be dipped in a solution called Electrolyte. It is liquid which is ionic and conducts electricity.
A simple cell
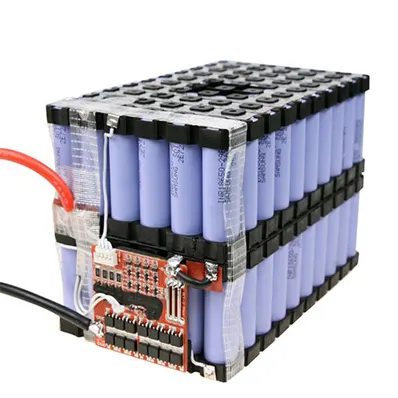
A 6 series and 10 parallel Battery pack example
Example Samples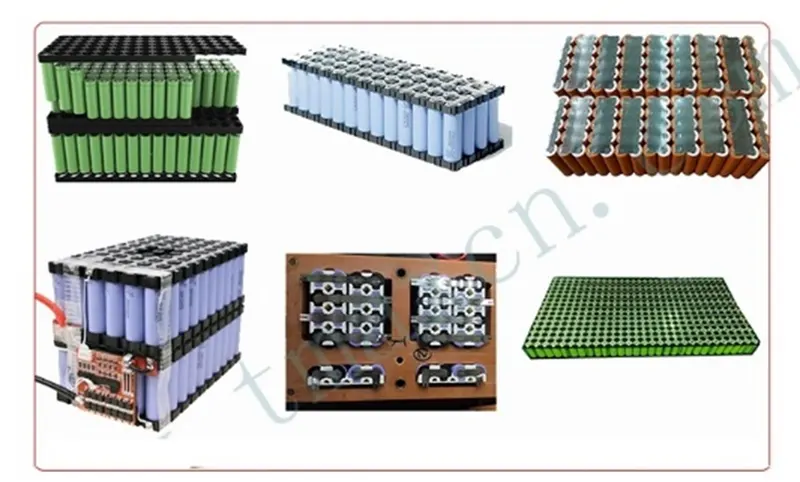
SUMMARY OF JOINING METHOS OF CELLS:-
|
Joining methods |
Advantages |
Disadvantages |
|
Resistance welding |
|
|
|
Laser welding |
|
|
|
Ultrasonic welding |
|
|
|
Mechanical joining |
|
|
Module level Joining
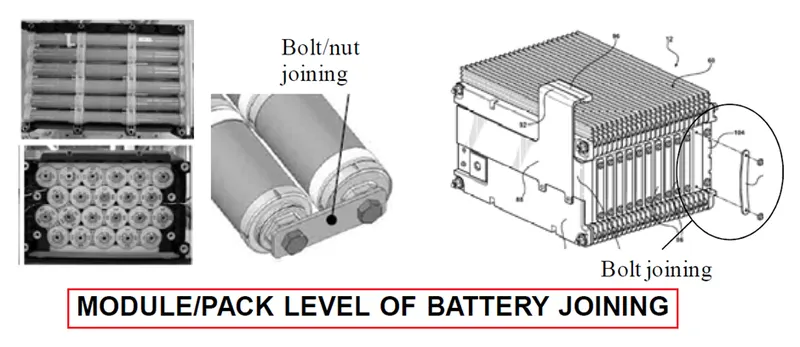
A simple six steps for battery Joining