Project 1
AIM: Route the wiring harness on given engine and prepare the flatten view drawing in CATIA V5.
Objective: This project involves the objective to route the wiring harness on given engine and prepare the flatten view drawing in CATIA V5 with all the necessary contraints applicable in Routing. All the packaging rules and indusrty best parctices shall be considered with necessary data of clearence , clipping/clamping section, Harness fixing requirements, harness continuity and assumptions of 3D data that is required to route the wiring harness on to a given engine.
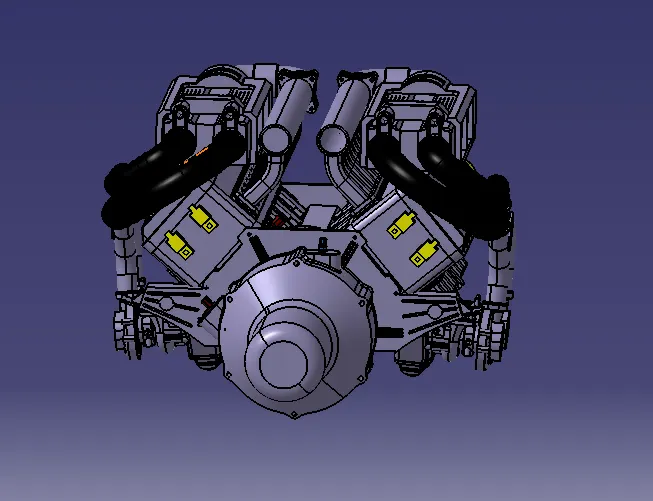
Fig 1
TECHNICAL SPECIFICATIONS AND ASSUMPTIONS:
- Wiring harness routing shall be ease in manufacturing, accessibility, maintainance and removal.
- Aviod routing through small structural holes, bolts, bolted joints, screwed joints to avoid harness puncture
- Provide additional slack to the harness according to the surrounding and harness bending requirements.
- Provide additional slack to the harness branch which connects to the loads and covered with enclosures.
- Avoid routing near sharp edges or over the sharp edges, in case of non avoidable situations addtional protection shoud be provided.
- Ensure harness is routed atleast 100mm away from ABC pedals.
- Enough clips and clamps shall be privided to ensure the positive clearence with surroundings and safety of wiring harness.
- Harness should be kept away from engine lifting hooks.
- Keep the harness away from engine heat generation components, heating lines and EGR components.
- Avoid direct support of harness on fuel lines routed in engine, in that case a seperator clamp to be provided to satisfy clearence requirements.
- Harness branch length should minimum 50mm.
- Minimum distance between clip and nearest branching point should be 25mm.
- Limit the number of branches from single branching point to 4.
- Harness Protection should be provided according to the surrounding temeperature.
The v16 engine has 16 fuel injector sensors, 4 cam shaft sensors, one coolant temperature sensor, 1 speed detection sensor, 1 neutral sensor.
4 pole connector is used for injector sensors and cam shaft sensors, so in total of 20 4 pole connectors are used which is shown in the fig 2.
2 pole connector is used for rest of the sensors which is shown in the fig3
One guiding channel top and bottom should be used on either side of the engine for in the high temeperature region which can withstand up to 150deg C.
P clamps are able allow the bundles to pass through it are used.
Fir tree clips which provides the proper support to the bundle and avoid fouling are used.
20 pole interconnection connector with cavity is mounted on L bracket from where the connections of bundles goes through out the engine is used.
CONTENTS:
Step1: Creating Engine harness context assembly and Geometrical assembly
Engine harness context assembly contains 3D data of engine assembly and all the non electrical data are stored in it and also the geometrical bundle assembly which consists of the electrical data needed for the project
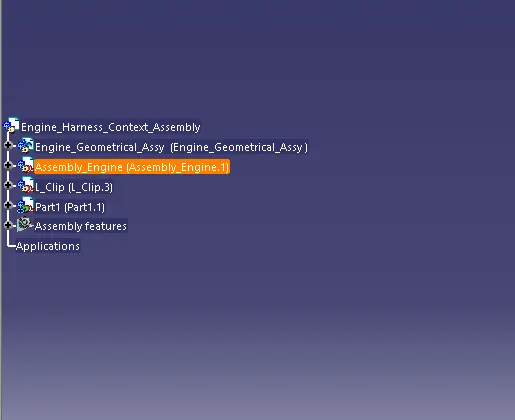
Fig 2
Step2: Defining 4 pole and 2 pole connectors electrically.
The 4 pole connector C-1563689-1 used for injector sensors and cam shaft sensors and 2 pole connectors namely C-173090-2 and C-282080-1 are respectively used for Neutral sensor & Speed detector sensor, Coolant temperature sensor are desined electrically with all the bundle connection point and connector connection points.
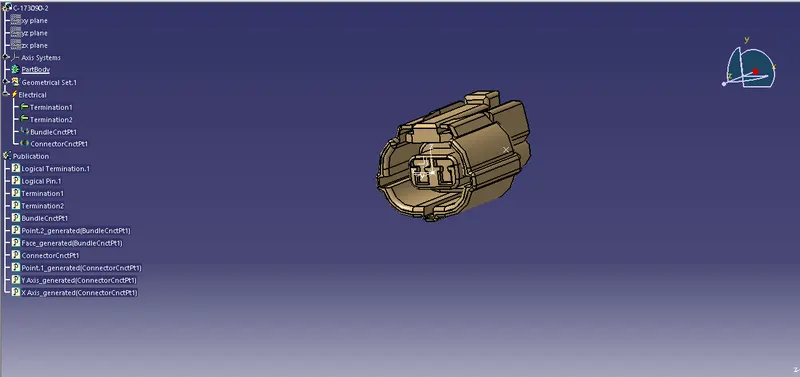
Fig 3
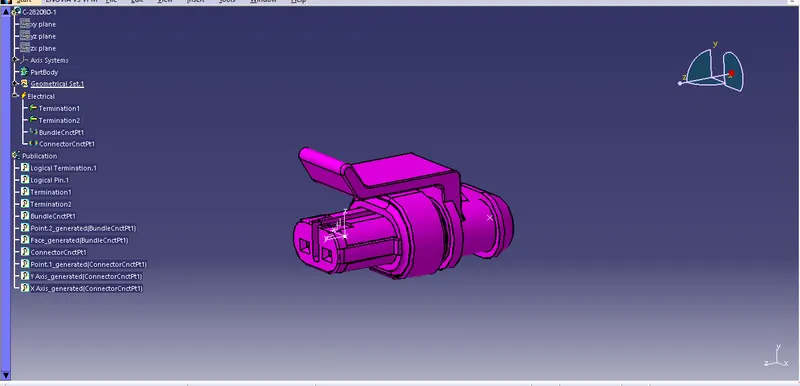
Fig 4
Step 3: Adding 4 pole and 2 pole connectors to Injector sensors, cam shaft sensors and Neutral and Speed measurement sensors respectively as shown in the diagram below.
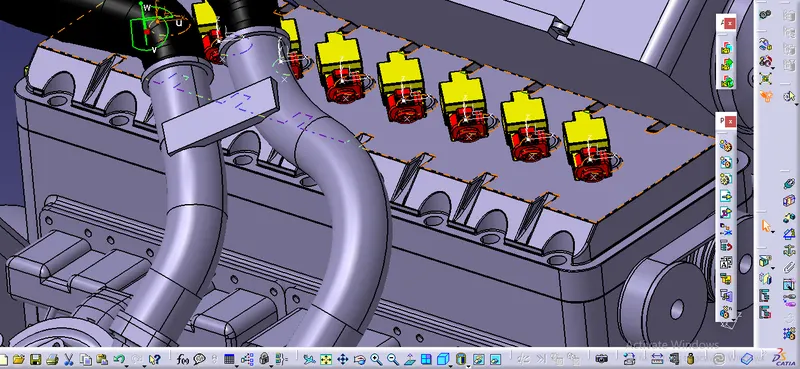
Fig 5
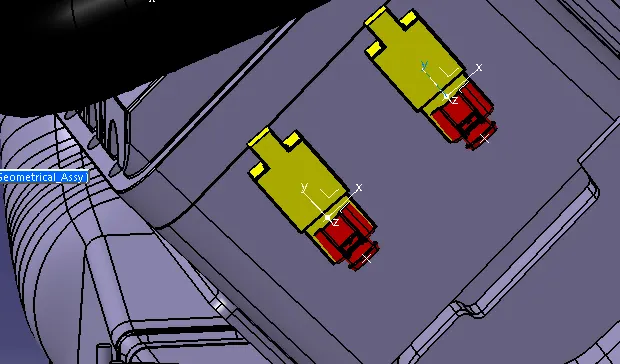
Fig 6
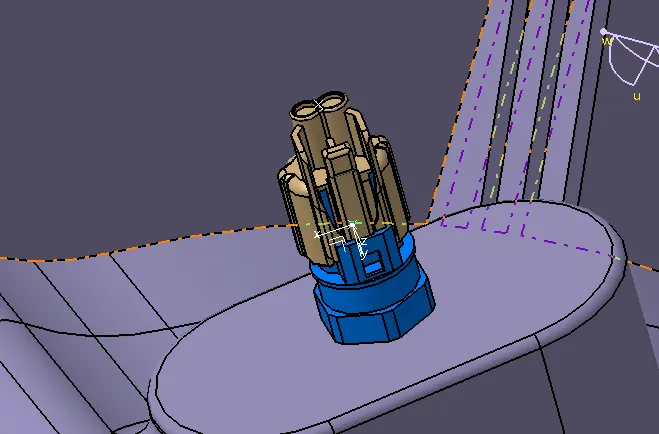
Fig 7
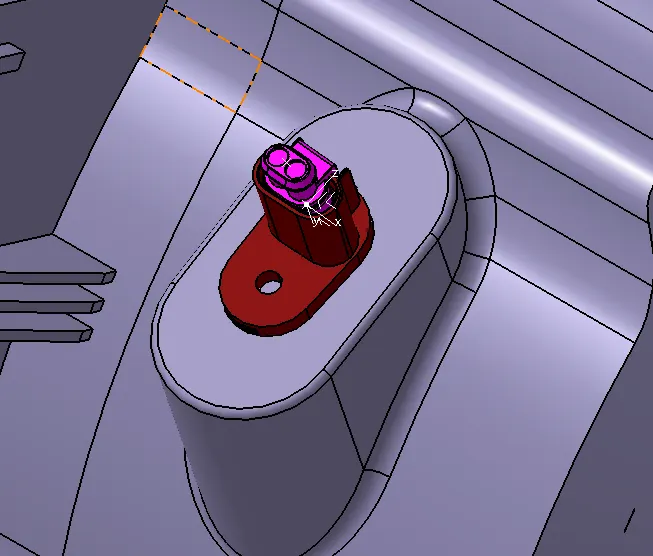
Fig 8
Step 4: Defining and mounting P clamps and fir tree clips on to the mounting joints
P clamps and fir tree clips are defined electrically by creating bundle entry plane, exit plane and base plane as shown in the fig and defing it as support part. Once both of these are defined electrically mounting begins on to the engine assembly in the suitable spots as shown in the fig.
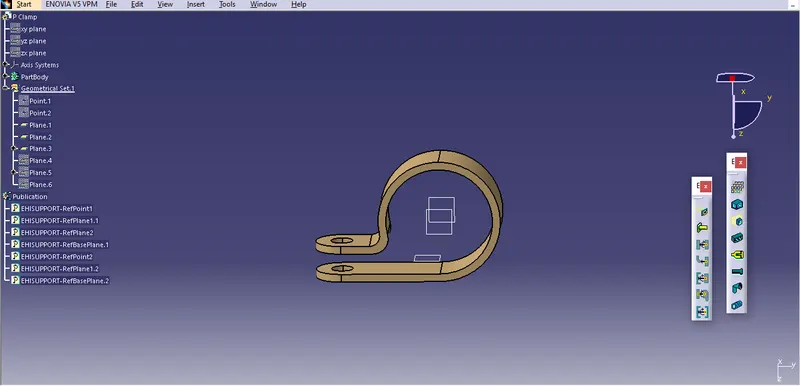
Fig 9
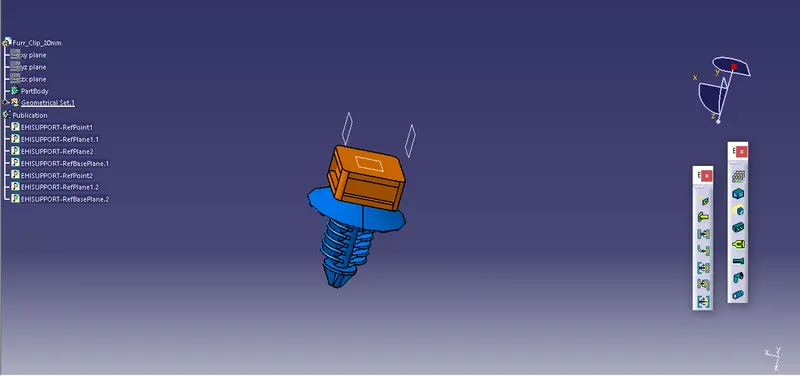
Fig 10
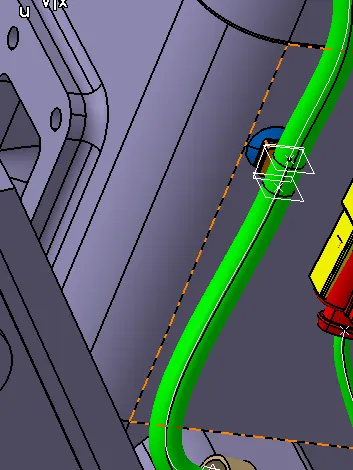
Fig 11
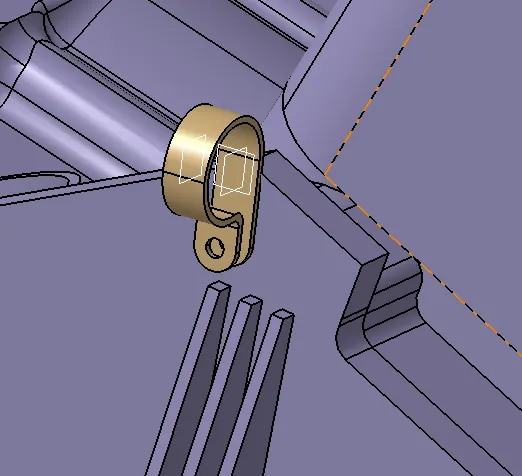
Fig 12
Step 5: Adding Plastic guiding channels and defining it electrically
We have 8 fuel injectors on the right and 8 on the left which are very close to each other in very high temperature zones, so the best way to route to these injectors is through plastic guiding channels both on the right and left side to avoid the complexity. The guiding channels are designed in such a way that a proper guiding holes for mouting should be available.
A min clearence of 50mm is to be provided between guiding channels and exhaust pipes.
To make path for bundle routing an external curves along the path of routing should be created as shown in the fig below. Now the guiding channel is place and mounted near the 8 injectors using manipulation tools and compass and it should defind electrically as equipment and will be a part geometrical bundke assembly
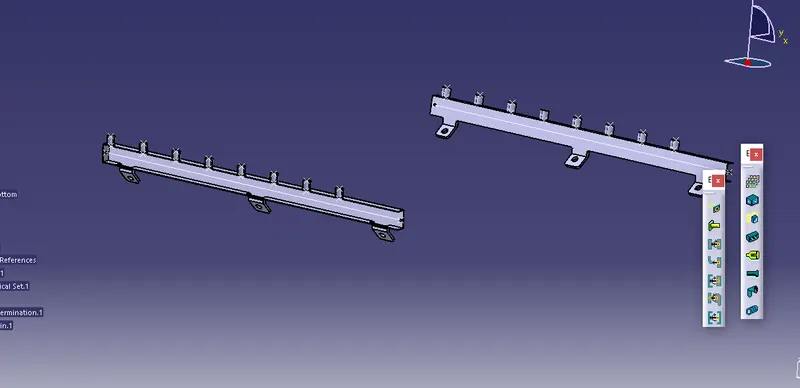
Fig 13
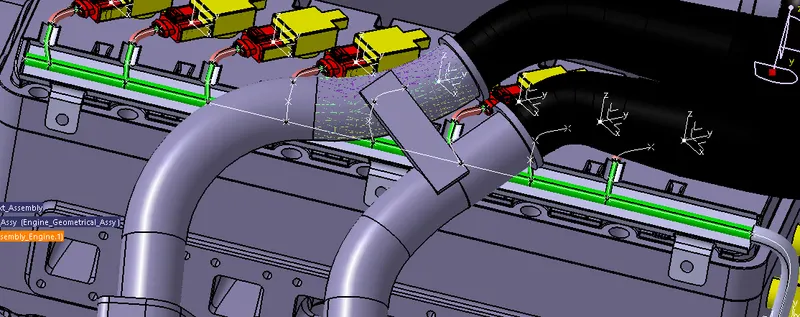
Fig 14
Step 6: Defining Interconnection connector and cavity and mounting it on L bracket
The Interconnection connector used here is C-776438-4 12 pole and cavity used for this connector is C-1924487-2 are defined electrically with all the bundle entry points connector connection points and cavity connection points and connected electrically and mounted on the L bracket which is in turn mounted on the engine assembly as shown in the fig.
The bundle routing starts from interconnectio connector.
Avoid sharp edges in the L bracket to avoid the puncture of harness bundles.
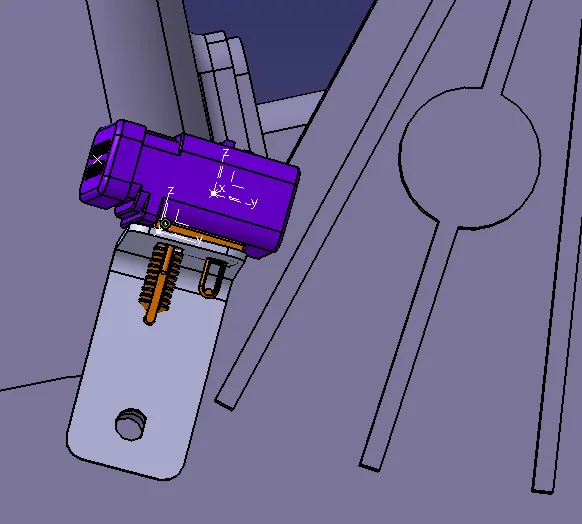
Fig 15
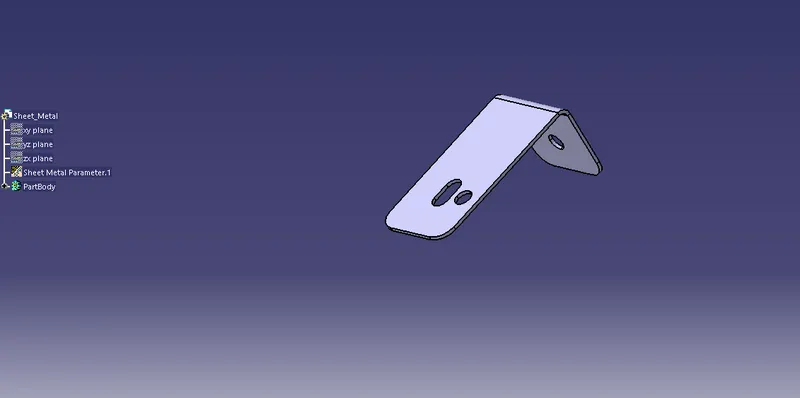
Fig 16
Step 7: Bundle routing from interconnection connector to all the connectors arranged and all the mounting parts
The dimensions assigned for bundles, like diameter and bend radius are assumed and actual values are provided at a later stage
From the below figure it is seen that the routing starts from the interconnection connector and goes in to all three P clamps
The bend radius for all the bundles is assumed to be 1.4mm
Step 8: Creating branching points in the bundle to connect CAM shaft, Neutral and Speed sensors
The branching points are added at a suitable place between P clamps which is best suitable for bundle to connect all the sensors as shown below.
Additional slag to be added for for the end connectors to avoid the tension in bundles which may lead to breakdown
The below two figures shows the branching points and bundles connecting from these points to connectors.
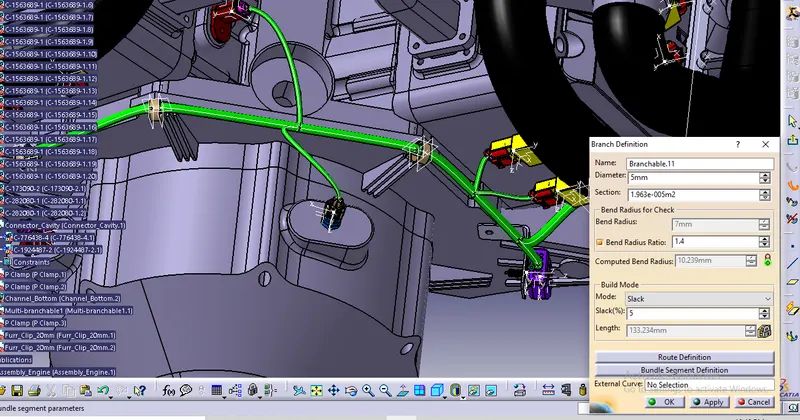
Fig 17
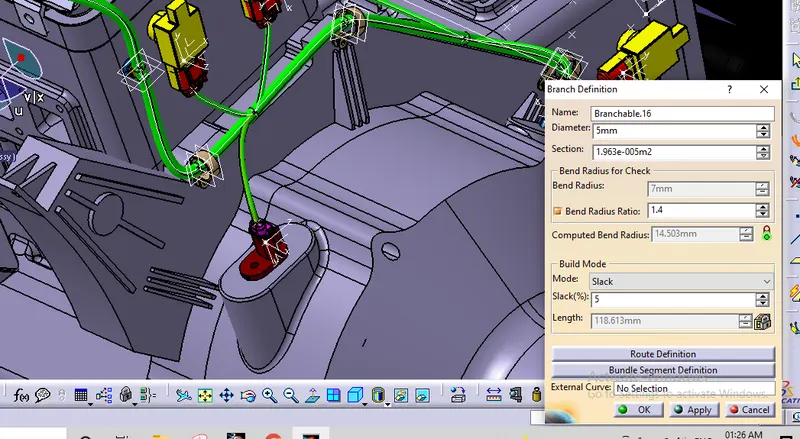
Fig 18
Step 9: Routing through guiding channels and from guiding channel to Fuel injector sensors
Routing through guiding channel is done through extenal curve and points that are created in an external geometry, from the guiding channel outgoing terminals the bundles are connected to 8 fule intector sensors on either sides as shown in the below figures.
Fig 19
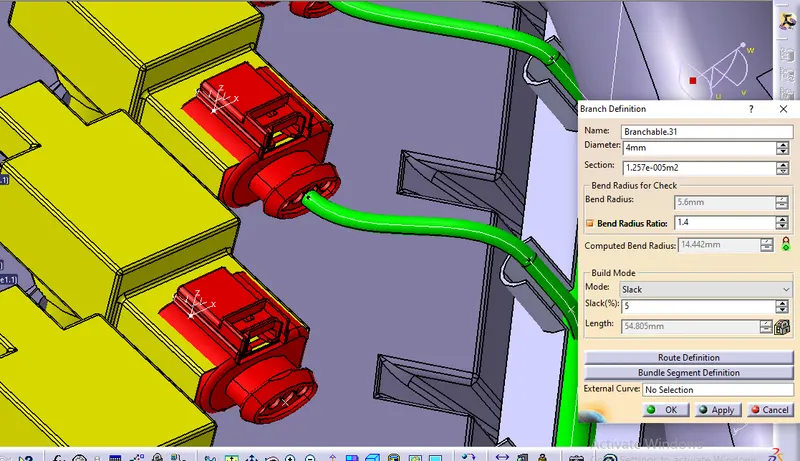
Fig 20
A complete view of geometrical bundle assembly after all the rounting and connections as shown below
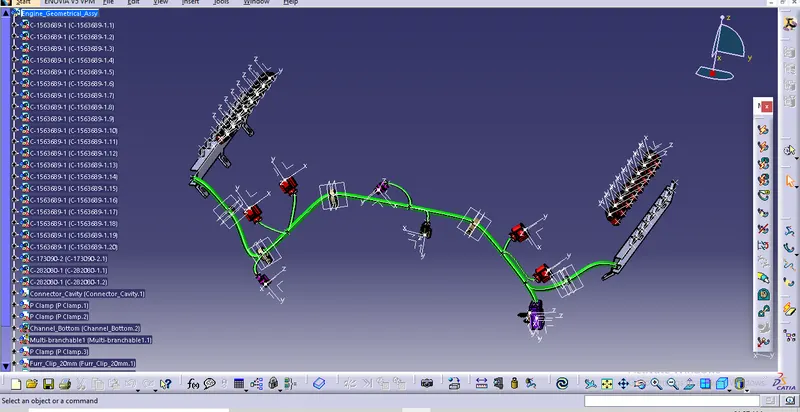
Fig 21
Step 10: Add protective coverings to the bundles
Corrugated tubes of dia 12mm are added on to the 10mm bundles and 5mm COT tubes are added on to the 4mm bundles connecting the connectors which are in not so hot regions and 5mm cotton tape is added to the bundles connecting fuel injector sensors which usually have a surrounding temeperature up to 150 deg C as shown in the below figures.
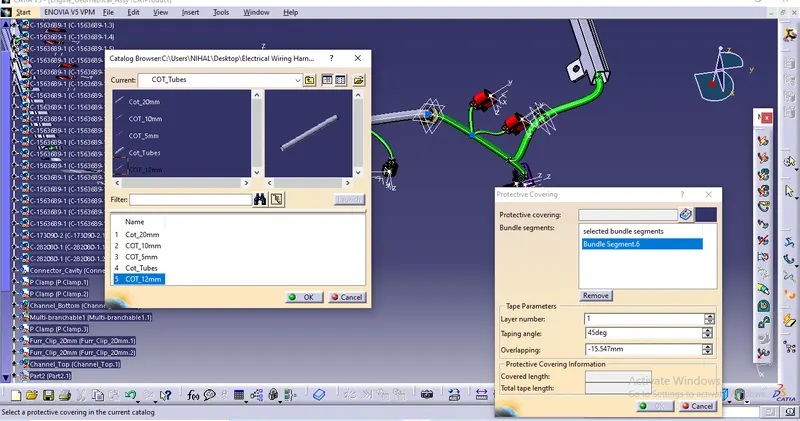
Fig 22
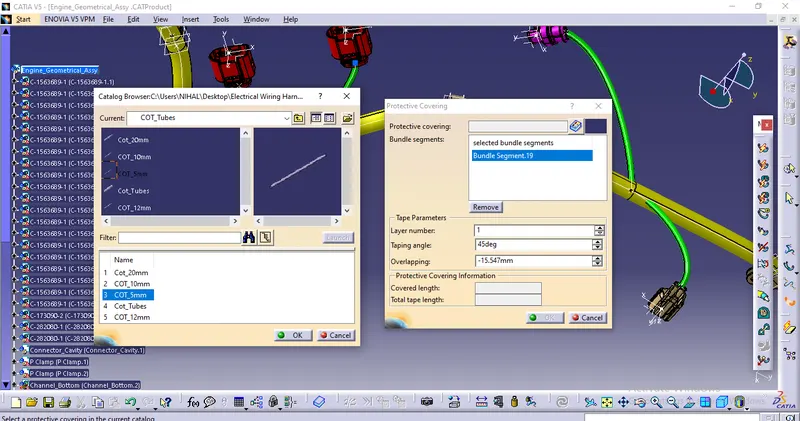
Fig 23
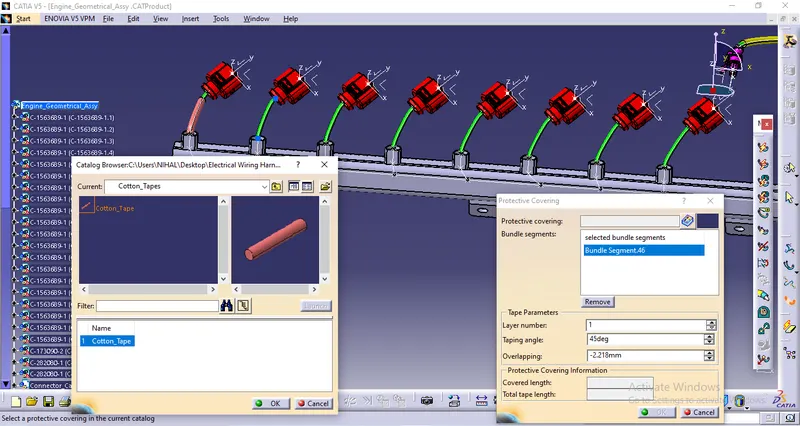
Fig 24 - Cotton Tapes
Step 11: To check the bundle connectivity
Go to edit>Serach>Advanced>Electrical workbench>Type-Bundle segment>Attribute-Fully connected
Selecting True will show all the bundles that are in continuity and fully connected and False will the non connectivity of bundles
When selected true all the bundle segments are found to be fully connected, as shown in the figure below.
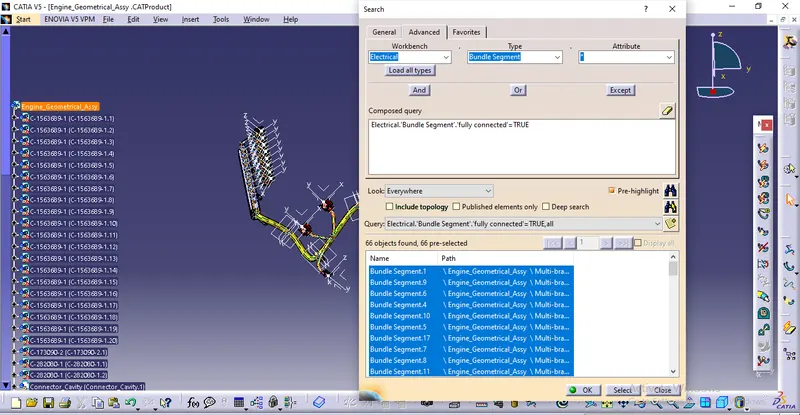
Fig 25
Step 12: Creating flatten product and Flatten drawing view of harness assembly
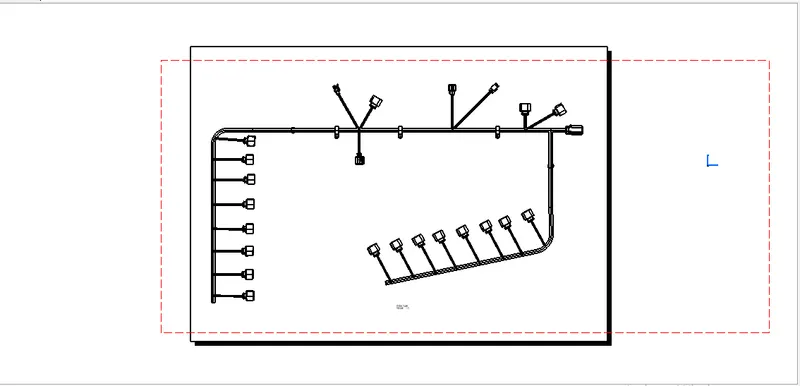
Flattened product is 2D representation of harness bundles along with all the electrically defined equipments to present it on piece of drawing paper.
To create flattening product of the assembly working bench should be Electrical harness flattening, name the new product as Engine harness flattening product and define flattening parameters as shown in the figure, and make sure to use single line foe bundle and double line for COT tubues and cotton tapes for better differentiation.
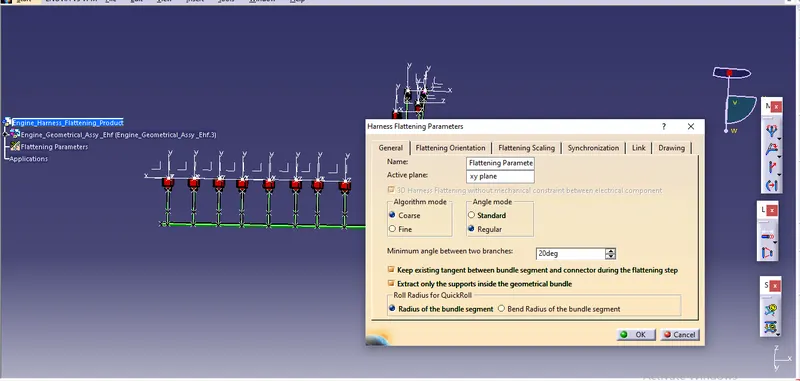
Fig 26
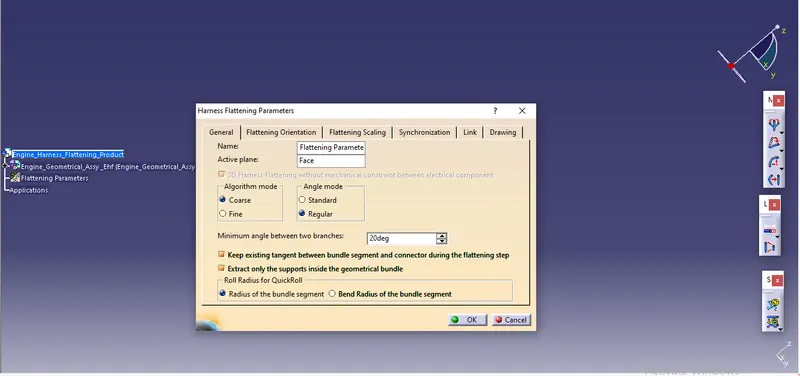
Fig 27
Once the parametrs are defined , the geometrical bundle assembly should be extarcted in to the flattening product by using the extract option in the work bench. Once the assembly is extracted use the flatten option to flatten the entire assembly.
Fig 28
Once the flattened product is obtained make all the necessary changes like scaling, rolling, rotating, straightening etc. Now transfer the flattened assembly on to the 2D drawing sheet by creating new drawing sheet and save the drawing sheet in the same location as all the files saved before.
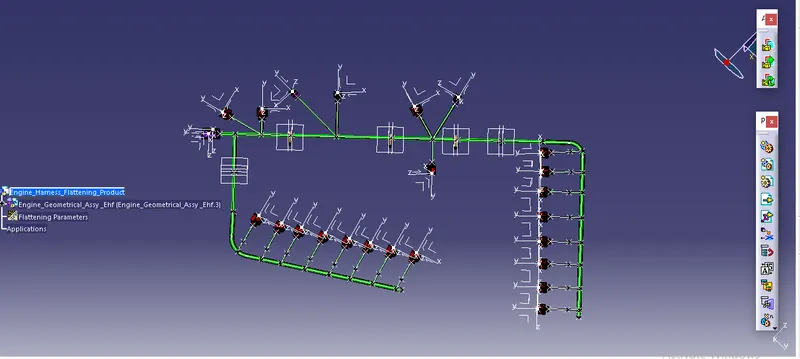
Now select the front view option and select the plane of the flattened which was selected earlier in the flattening properties.
Now the 2D diagram of flattened model is displayed on the drawing sheet, now to go the that drawing properties and in the view section make sure 3D wire frame is always ON which represents the bundles and make sure the graphic for device is 3D projection for better identification and understanding and single line for bundle and double line for protective coverings, and 3D colors can be added for better look as per the image shown below.
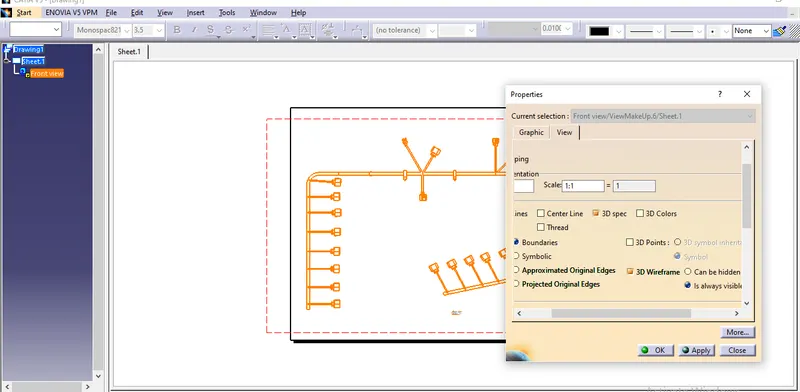
Fig 30
Final 2D harness assembly is shown in the below diagram.
Conclusion:
Routing of wiring harness for V16 engine is done and flatten view for harness assembly is created in CATIA V5. In the process of this project various packaging rules and constraints are considered for routing the wiring harness. Industry best practices are considerd while designing wiring harness. Every minute details and major details like clipping and clamping section, Clearences, harness fixing requirements, bundle continuity are all considered in this design process.