Hood design-Week 2
Aim :-
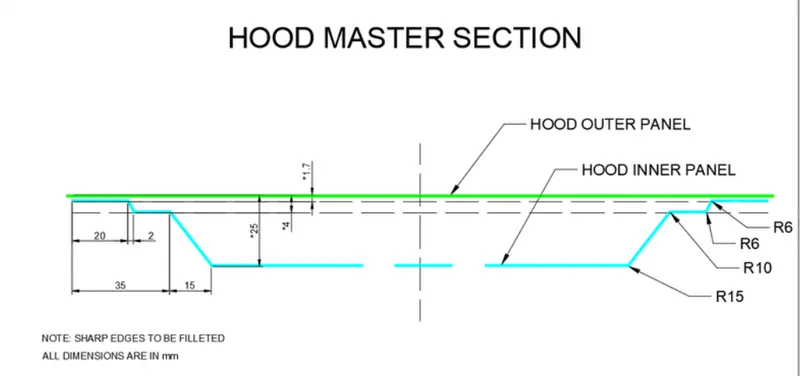
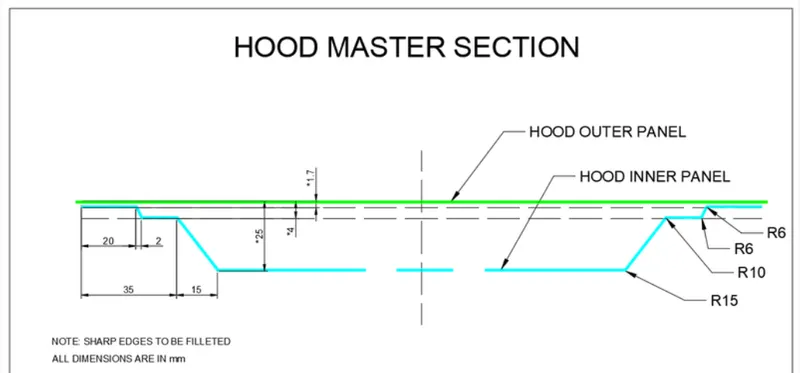
Design Hood Outer Panel, Inner Panel and the necessary reinforcements by following the Master Section mentioned with the Design parameters
Introduction:-
This project will make you understand about the hood of a car, explain some sheet metal operations that are commonly used in design and take you to the step by step procedure of designing hood components like its inner panel, outer panel, reinforcement and setting the trajectory of striker. Designing of the model is carried out in Siemens NX-12 here.
Hood –
The hood (north American English) or bonnet (commonwealth English) is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment or trunk on rear engine and some mid-engine vehicles for maintenance and repair.
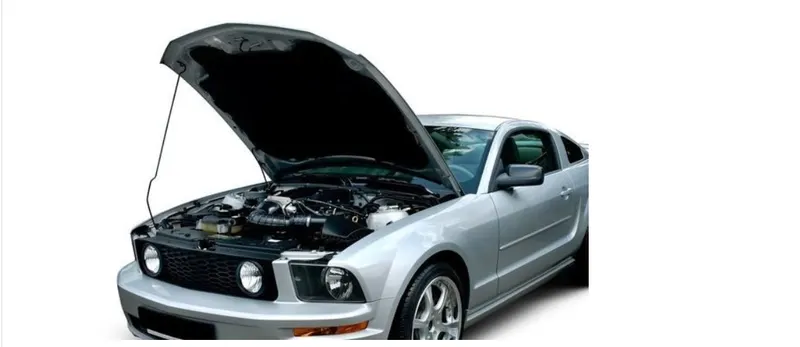
On front engine cars the hood may be hinged at either the front or the rear edge or in earlier models it may be split into two sections one each side, each hinged along the centre line. Hood are typically made out of the same material as the rest of the body work . This may include steel, aluminium, fiberglass or carbon fibre. However some after car market companies produce replacements for steel hoods in fibre glass or carbon fibre to make the vehicle lighter.
Hood is typically supported by rods or some fixture, so that it stays at a position and a person can lean onto it hassle free and work. These includes
Support rod : A hood rod is designed to hold your hood propped open whenever you need to do some work in your cars engine bay. When used it must be firmly secured to ensure that it provides a stable hold on the hood. Meanwhile when not in use it must be kept stable in place and must not move around. The hood rod clip is the part assigned with that function. This clip clamps onto the rod and ensures that it is firm in its place when not In use. It keeps the rod from moving around under the hood and from causing trouble.
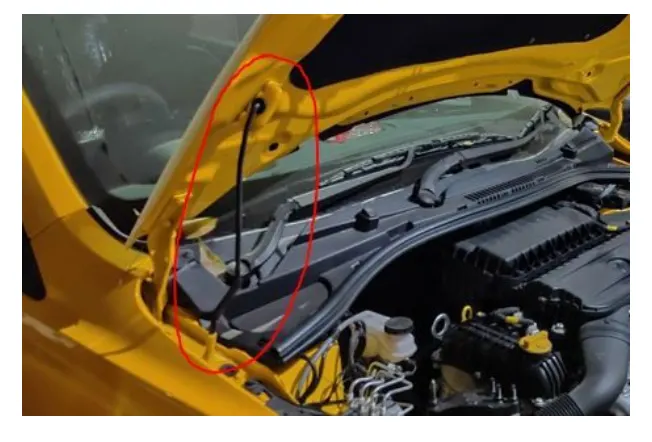
Gas Stay:-
This is used to open the car hood by just providing little lift force. A small effort is all it needs and other work is done by gas pressure. It is normally found in high end cars where mass of hood is more than normal.
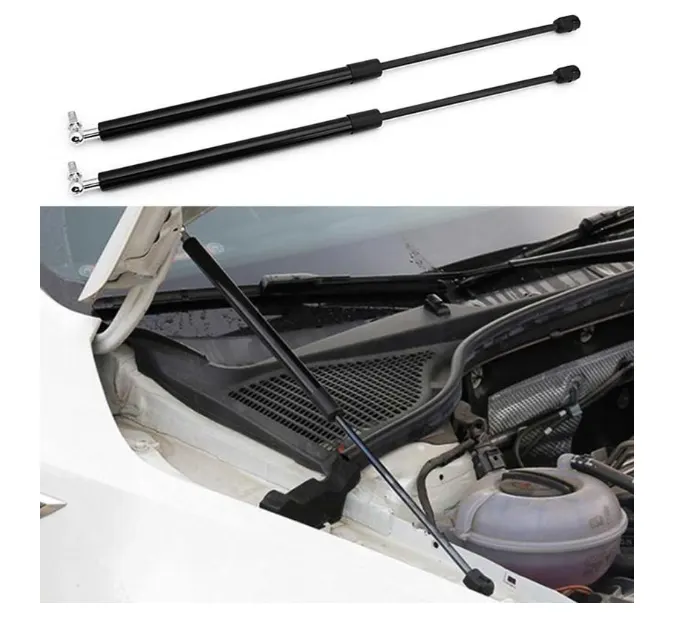
Sheet Metal Operation:-
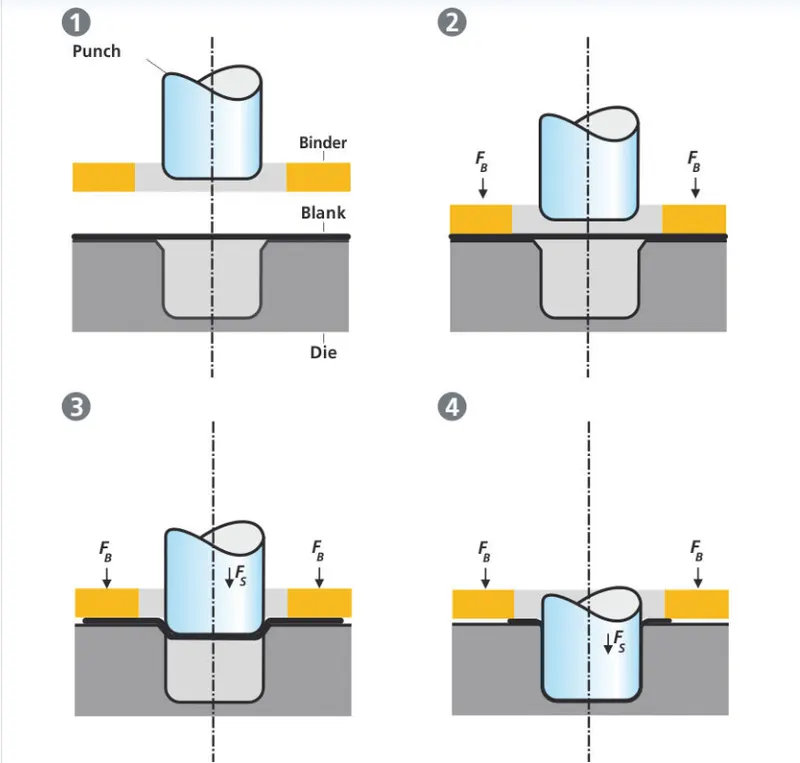
Deep Drawing: - Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered deep drawing when the depth of the drawn part exceeds its diameter.
Embossing:
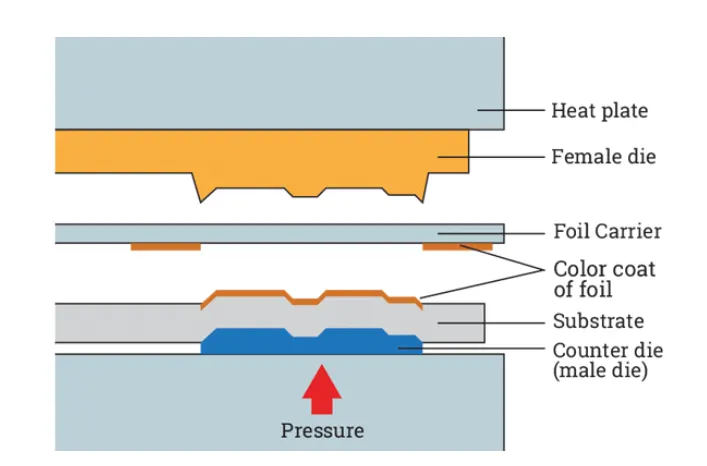
Sheet metal embossing is a stamping process for producing raised or sunken designs or relief in sheet metal. This process can be made by means of matched male and female roller dies or by passing sheet or a strip of metal between rolls of the desired pattern.
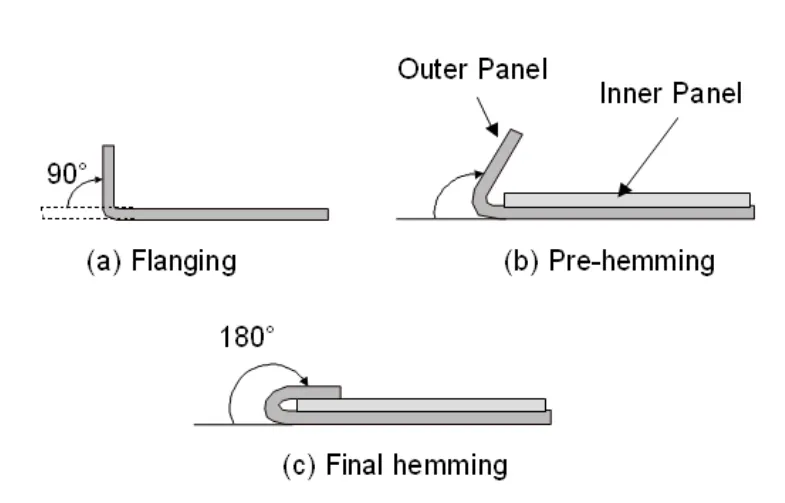
Hemming: Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together to improve the appearance of a part and to reinforce part edges.
Mastic Points:-
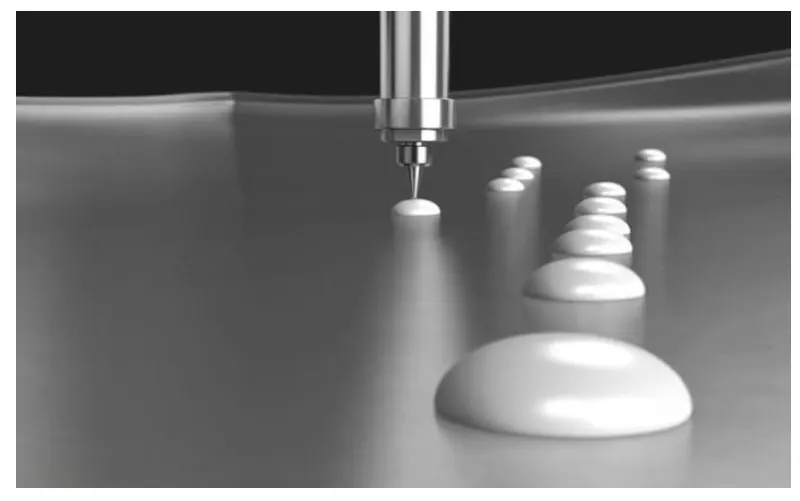
These are the spots where the inner panel and the outer panel of hood are joined or can say sealed together using a mastic glue. To fix the outer panel, if process like bolting, riveting, or welding is used it will lose all its aesthetics. So mastic sealant is used which is elastic compound and acts like rubber. It is placed between both the panels.
Parts of a Hood/Bonnet:
- Hood outer panel
- Hood inner panel
- Hinge assembly
- Latch and striker
Design Approach is carried out in a most effective way and step by step procedure is explained. The master sketch of the panel was already provided on the basis of which the inner panel is created here.
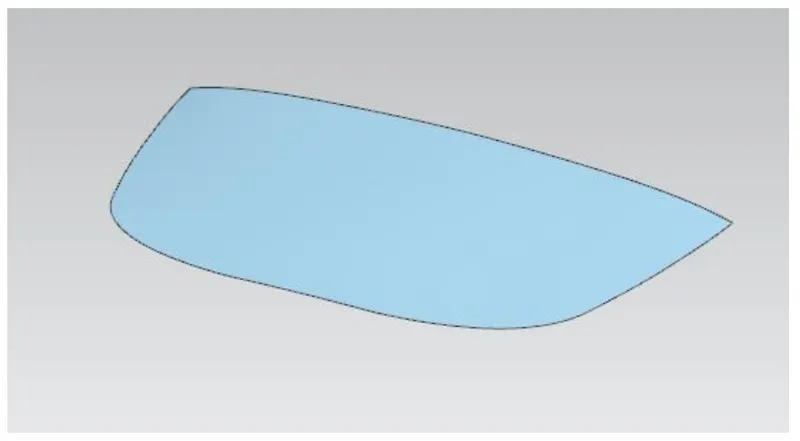
We will design the inner panel first, so let’s start with the given data, a body stretched to full dimension of outer panel.
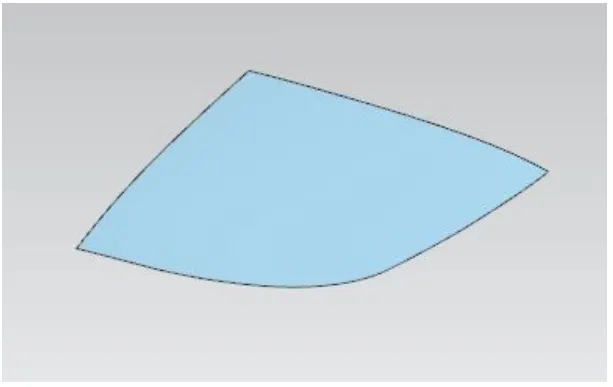
Next trim the sheet into half by trim command
Take a topmost surface offset and keep dimensions according to master section, i.e 2m
Taking curve offset on face 20 mm from outer curve
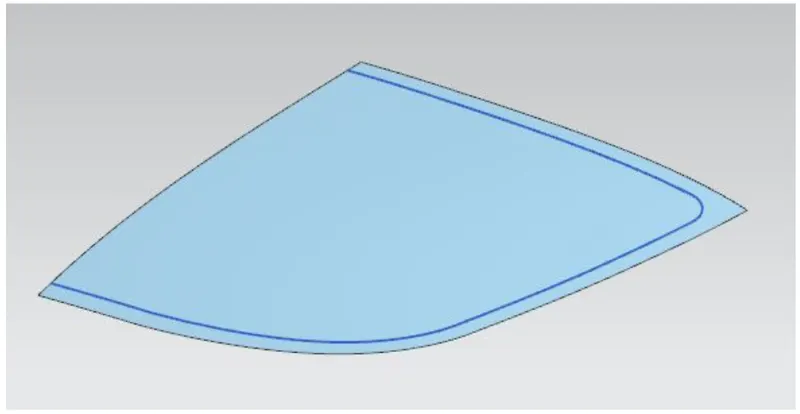
Trim sheet by using trim sheet command and keep the outer part
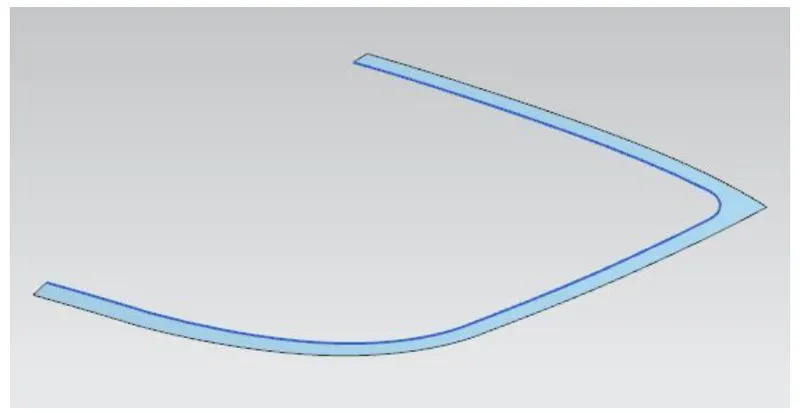
Take another 4mm surface offset from parent surface
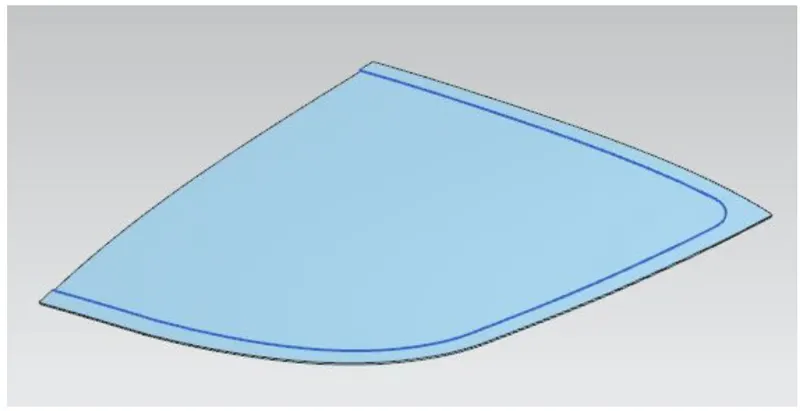
Now offset curve on surface same way for 40 mm inside.
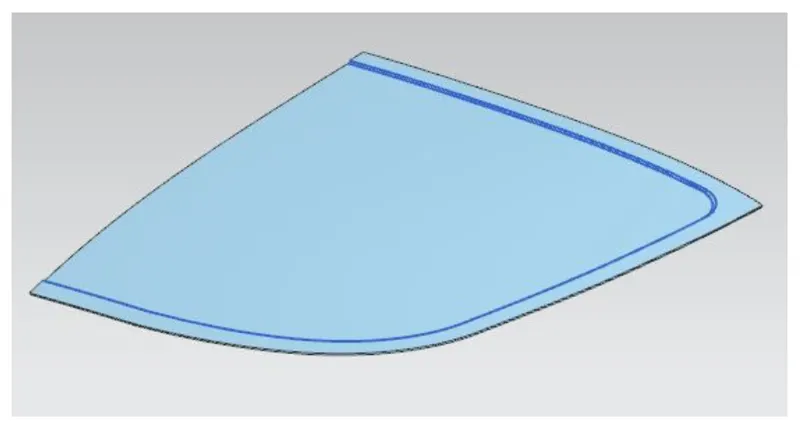
Trim outer panel of this sheet
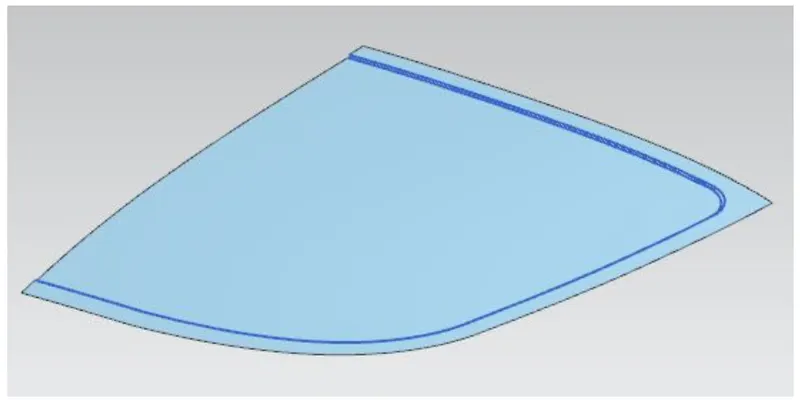
Now bridge the gap between these two sheets by using surface through command
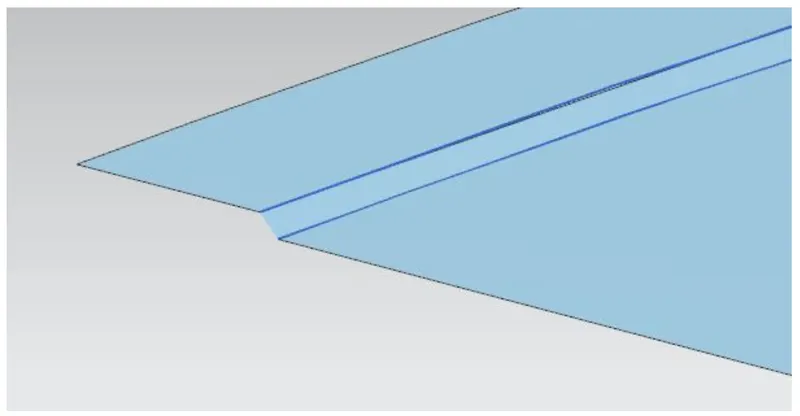
Take another surface offset from parent surface 25mm below.
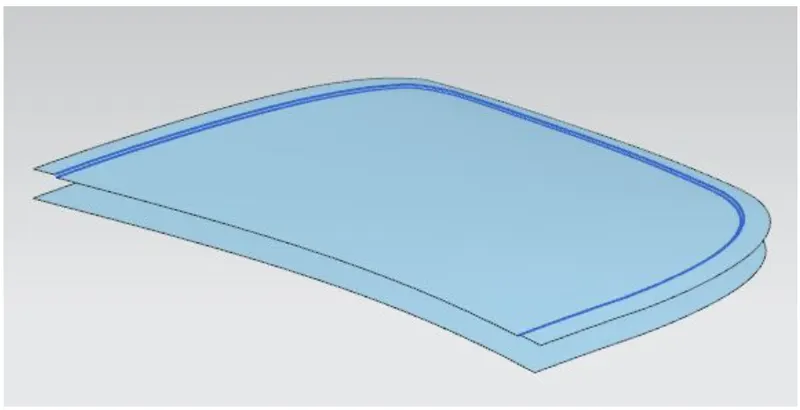
Do curve offset on surface 55 mm inside and trim sheet outer side by using trim sheet command.
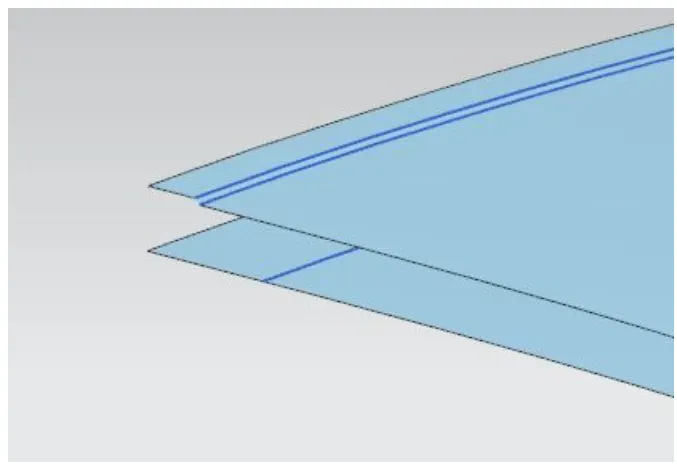
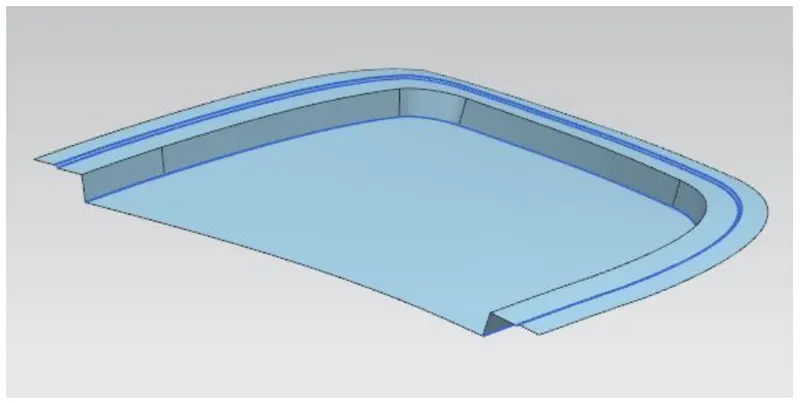
Now fill the gap we created surface by law extension command and keep draft of 10 degrees outward.
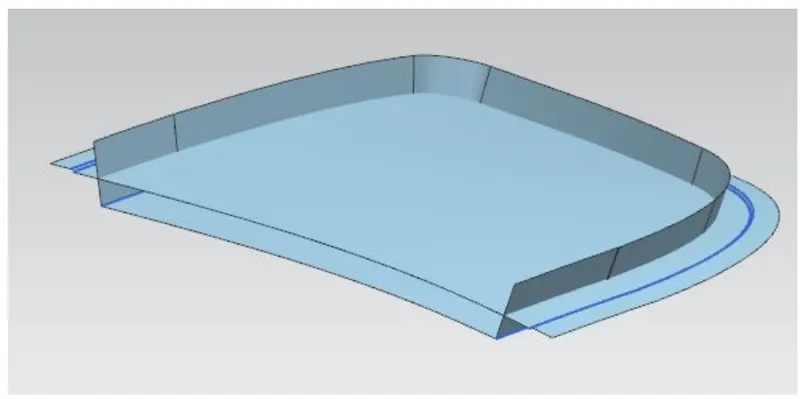
Using trim and extend feature we eliminate some part unwanted part and get this structure.
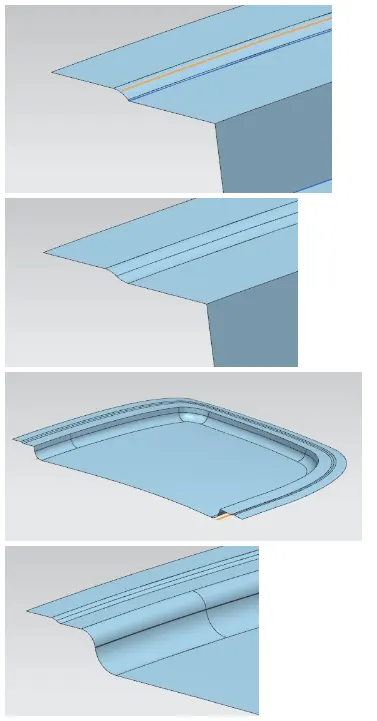
Now we will blend these sharp edges by edge blending and face blending by given dimension.
After blending we will create a sketch on XC plane on inner panel surface. We keep some space for hinge and striker.
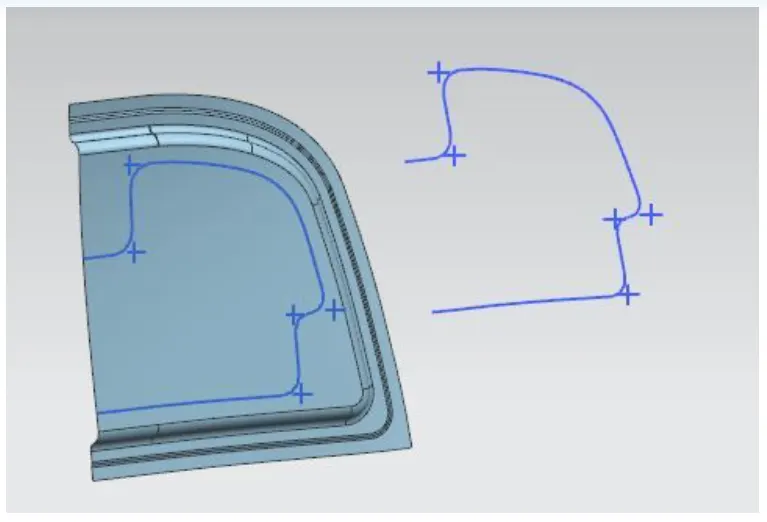
After finishing the sketch we projected these curves on surface by using project curve command and follow it by embossed command to create and emboss.
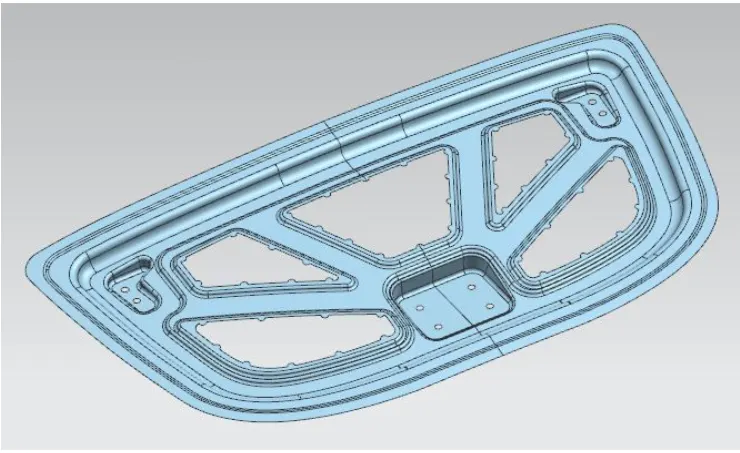
Same embossing procedure is followed to create and emboss
After creating emboss select the profile and trim the part.
Now we adjust the hinge assembly In position that we want.
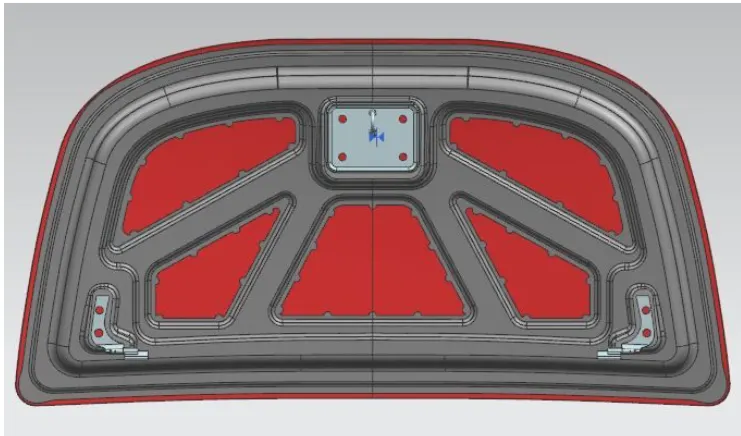
Now we create an emboss on corner to mount the hinge. Then create a dattum plane parellel to original dattum plane to give the offset to the hinge mounting eboss. So we get the flat and offset surface to mount the hinge
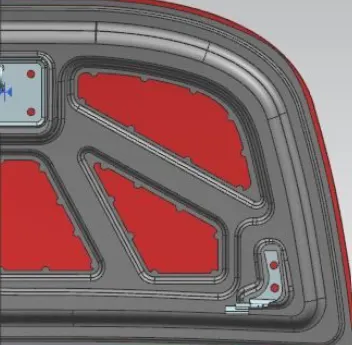
create a mirror of geomety by using mirror geometry command
Creat a emboss to mount striker but to know the exact position for strike we create a tragetry path and by using its tangent we find the position for striker
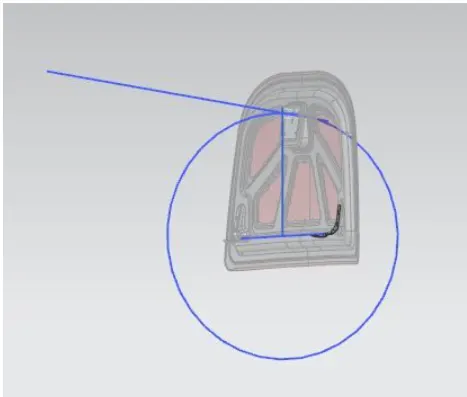
After succesfully creating tragetory path we use wave geometry linker to link the inner panel syrface and striker lower surface to match the position. Then create a geometry on inner panel surface to create emboss offset to the dattum plane. Now by using assembly constraint we give the touch to both (inner panel and striker) surface.
Now we thicken the inner pannel and outer panel by using thicken command by 0.75 mm
Now to join the inner panel and outer panel we used hemmings. So to create a hemming we follow the proceddure below.
Now select the outer panel. So we start with the same body as default and trim that into half
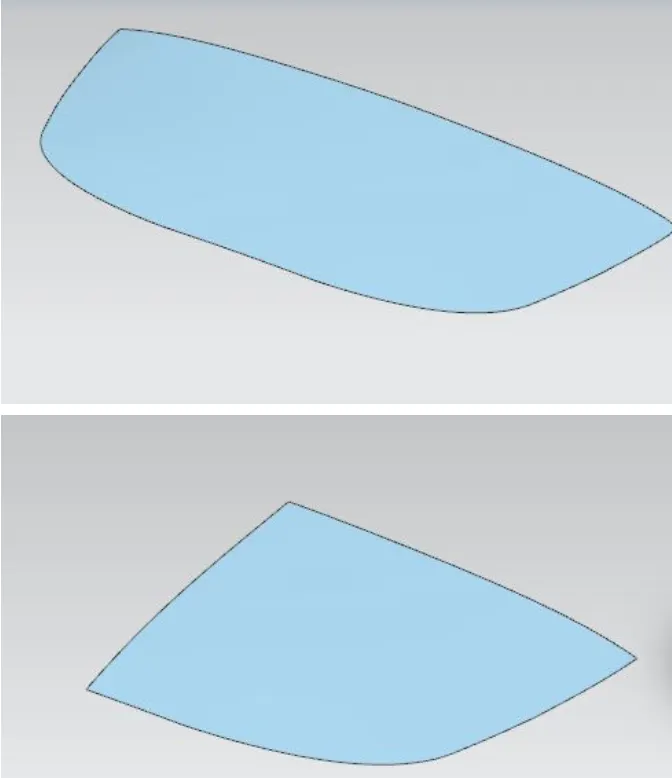
Take a curve offset and trim the part by 0.5 mm
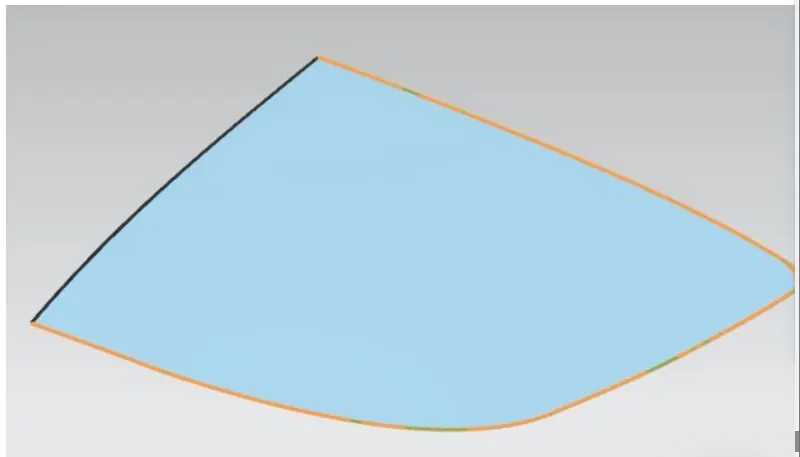
Extend the surface by law extension and keep darft of 5 degrees
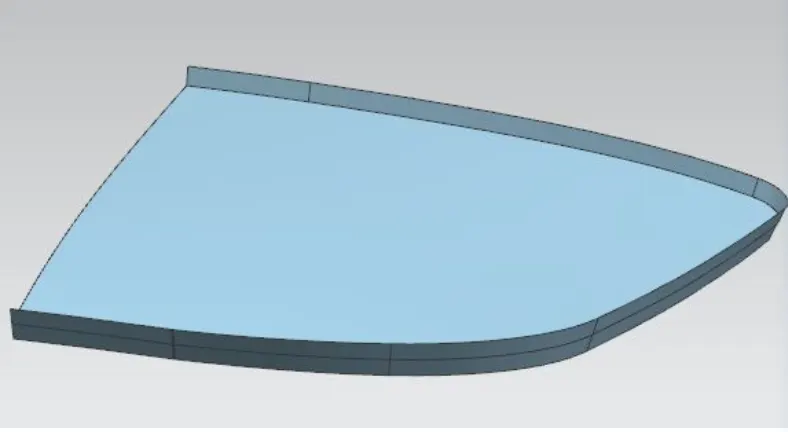
now take surface of both the surfaces available. Here for the law extended one we take 7.5 mm inside and for the workpiece we take 2.8 mm down (keeping the sheet thickness and gaps between them we are taking 2.8 mm)
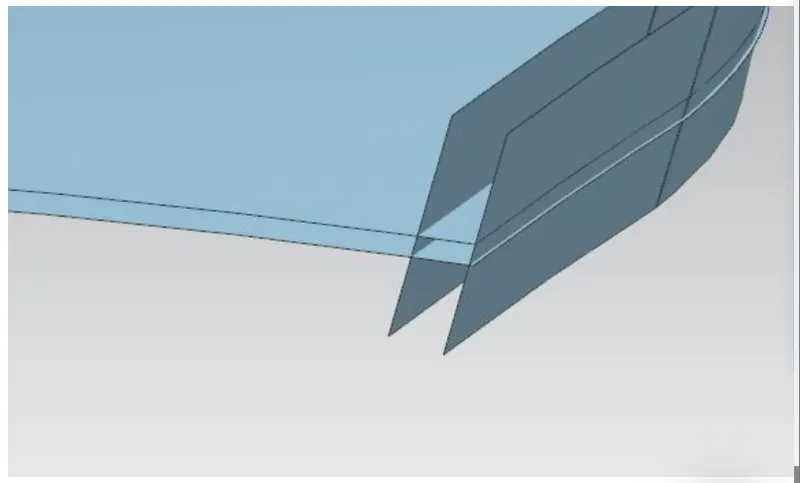
Trim the unwanted part of offsetted surface
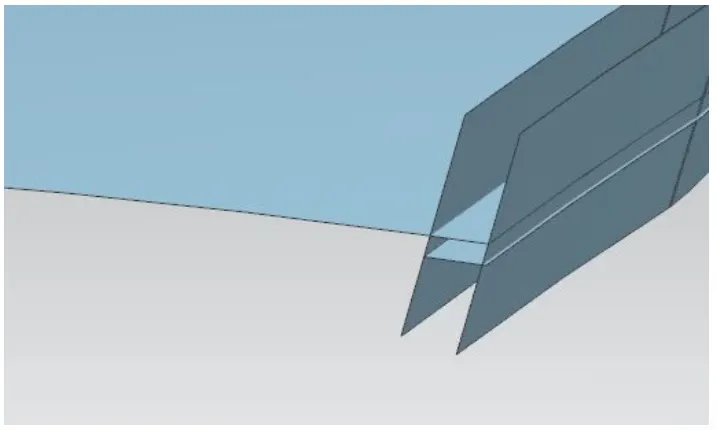
Now the hemming we keep some relief at the rear end and front end too.
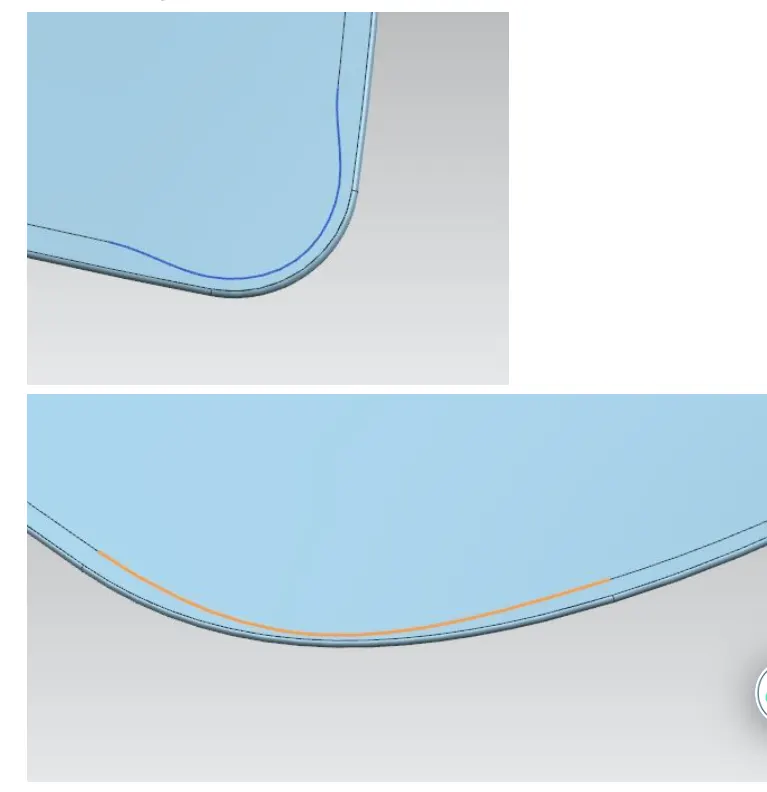
Now we can mirror the part to the plane and sew it.
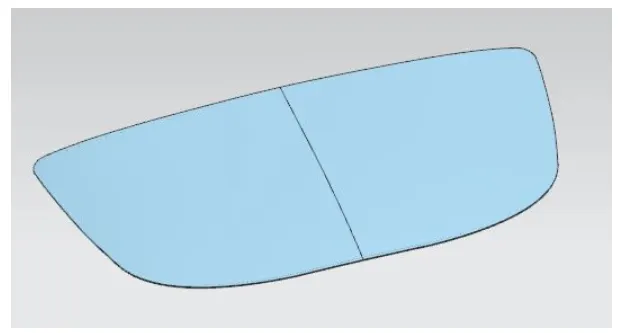
Now we get the final assembly like that
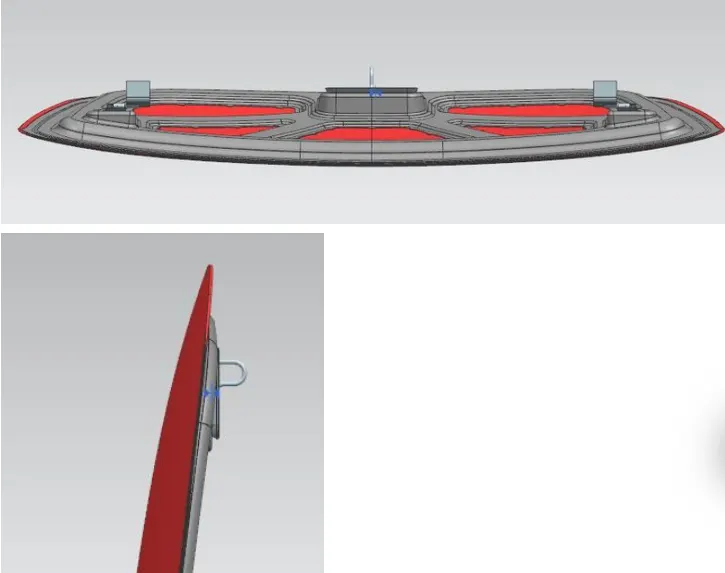
Conclusion :-
In this way by following the procedure, we designed both panels and set the striker trajectory and the reinforcements necessary and learned the features used in curves, surface and assembly and assembly in siemens NX.