Hood design-Week 2
Hood
- Hood is placed above the engine compartment, which can be opened to access for inspection, maintenance and repair. It is has two panels i.e., inner and outer hood.
- The inner hood panel gives strength to the outer panel and mounts it over front engine part with spot welding, gluing or with fasteners.
- Outer panel is to provide good style and look for the vehicle front portion and defines the aerodynamic of the vehicle. It acts as a critical safety component for the vehicle and pedestrian.
- Outer panel is joined to the inner panel through the hemming process.
- If any crash happens on the front side of the vehicle the hood needs to collide and reduce the impact passing to the pedestrian.
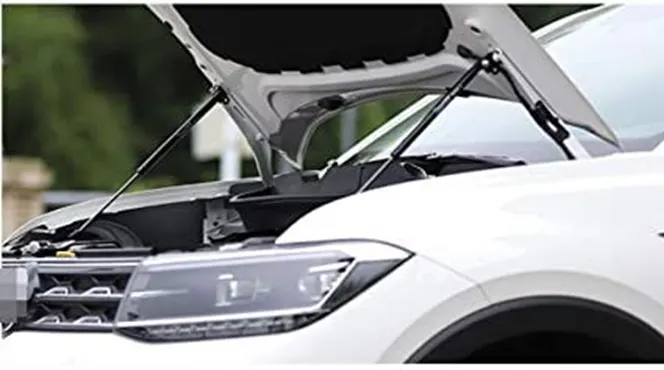
- While opening the hood, to support the opening and opened condition is achieved by the support rod and gas stay. support rod is manually opened and placed in the position with the rod inserted in the specified locker hole, while gas stay is automotive with the actuator will open the rod to the specified length.
Design Requirements
Design specifications for the automotive hood component.
- No negative draft angle
- Manufactured by Deep drawing process
- No sharp corners
Hood Thickness Information
- Outer Panel Thickness = 0.75mm
- Inner Panel Thickness = 0.75mm
- Reinforcement Thickness = 1.5mm
Design considerations
- Noise vibration harshness : caused by aerodynamic nature , mechanical components (engine, brake, tyre), electrical components (actuators, traction motors).
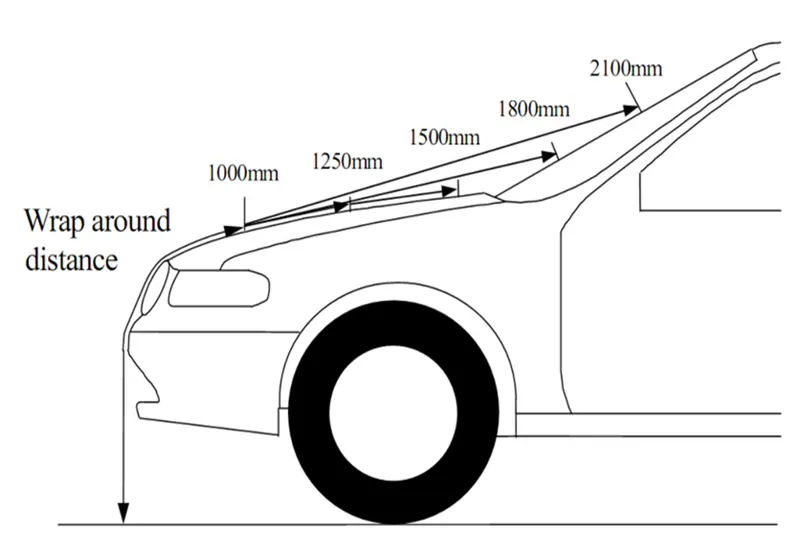
- Pedestrian head impact assessment : based on impact test area on wrap around distance, impact conditions like impact velocity and angle.
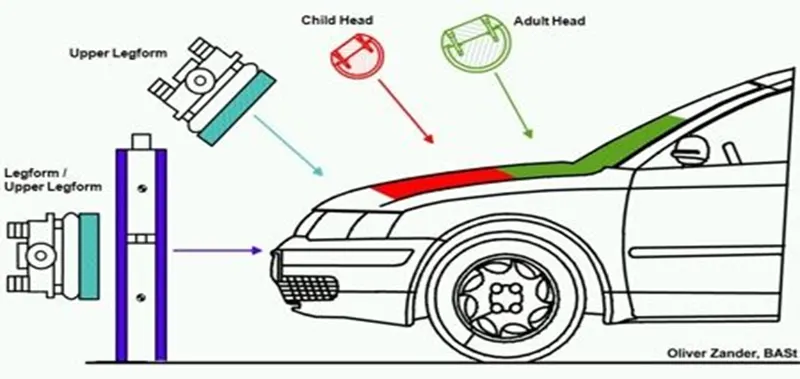
- Wrap around distance : The shortest line which connects the reference plane with any point on the vehicle, which passes through the vehicle's front and front's upper-surface.
- Head clearance zone
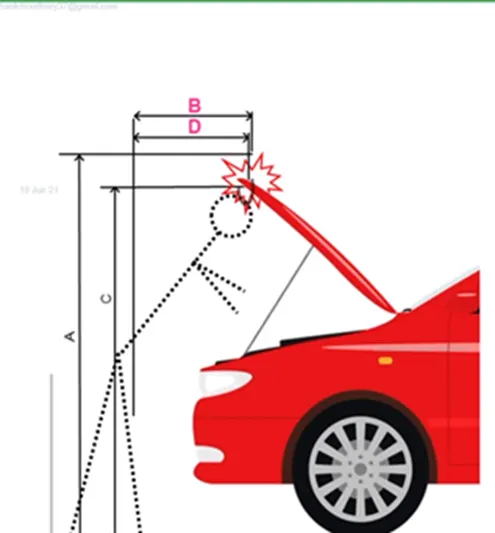
- EuroNCAP safety standards.
- Lock Stricker hood support rod accessibility
- Manufacturing feasibility
- Release mechanisms and safety aspects
Materials suggested
Aluminium, steel, carbon fiber reinforced plastic, glass fiber reinforced plastic.
Manufacturing process
The process involved in designing hood as a sheet metal operation is
- Deep drawing
- Hemming
- Blanking and Piercing
- Embossing
Deep Drawing
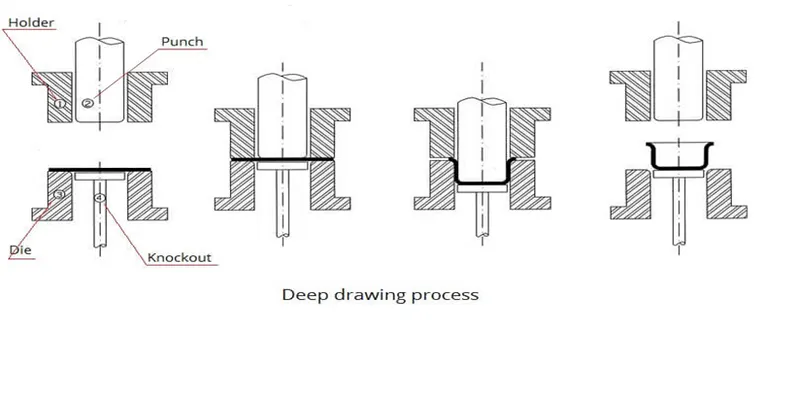
A deep drawing of sheet metal is performed by punch and die. The punch needs to be the desired shape of the base part. The die cavity should be exactly matching the punch and is a little wider to allow for its passage, as well as clearance of angle seven degree. Thickness is assumed to be uniform for this process.
Hemming
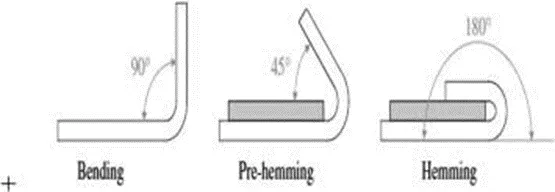
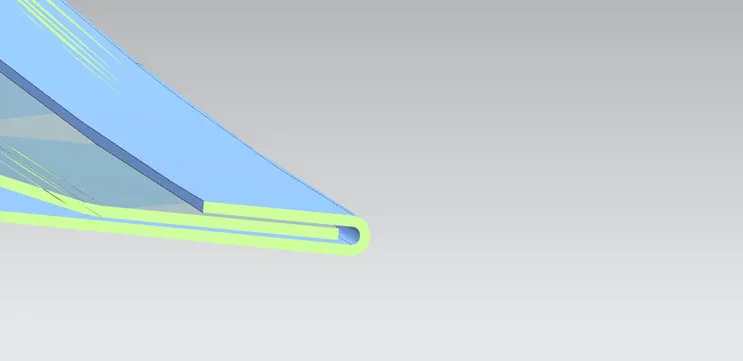
Hemming is a sheet metal forming process in which sheets are joined by bending like u shaped with an angle usually around 180 degrees.
Hemming is carried out incrementally with a hemming roller of different diameters as well as from different angles.
Hemming operation will be carried out sub categories with bending, pre-hemming, hemming, finishing and checking process. A relief angle is provided to corner of the sheet metals.
Blanking and Piercing
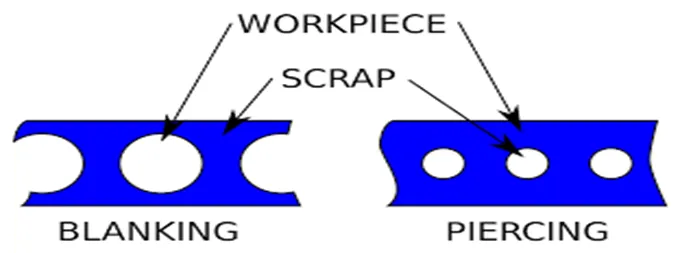
Blanking and piercing both are the sheet metal process in which punch and die is used to produce the parts. Blanking provides the outside features of the part while piercing provides internal profiles or holes.
Embossing
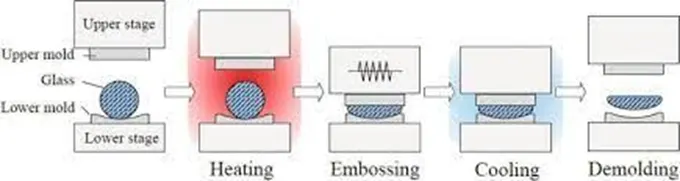
Embossing is the sheet metal process for producing the sunken design with the relief considerations. This process is carried out by matching the male and female roller dies by passing the sheet between the rolls by desired pattern.
Hood components and functions
Hood consists of major four components outer hood, inner hood, hinge,striker which is supported by the support rod and gas stay while in opening conditions.
Hood Design
Based on the design requirements of the hood design making the inner hood from the reference of the outer hood surface.
Hood outer panel
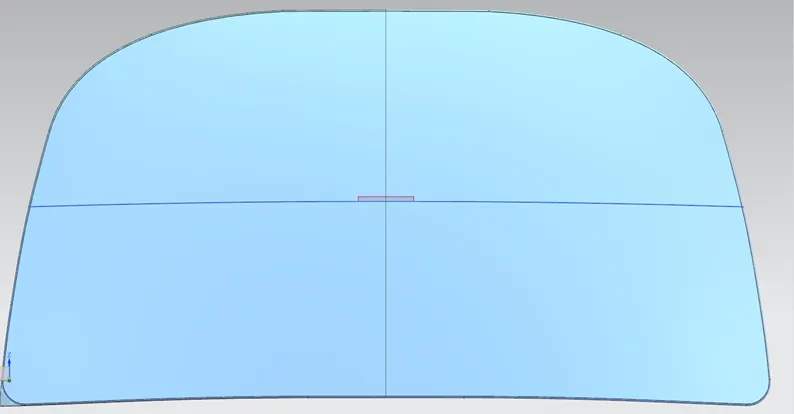
outer panel is the stylish bonnet which gives good asthetic look for the car. outer hood is provided with the distance of 0.75mm thickness and provided with the relief at the corners. It should also be deigned based on the satisfy safety norms.
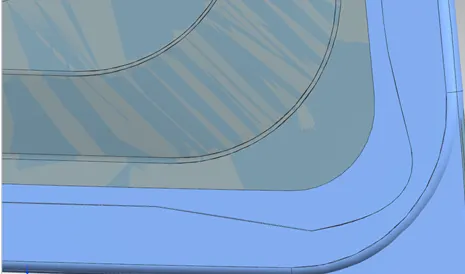
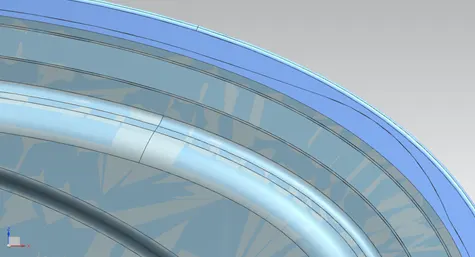
Reliefs are provided to reduces stress distribution on the corners as well to avoid the wrinkles, wall thinning,ovality and buckling.
Side Relief
Front Relief
Hood Inner Panel
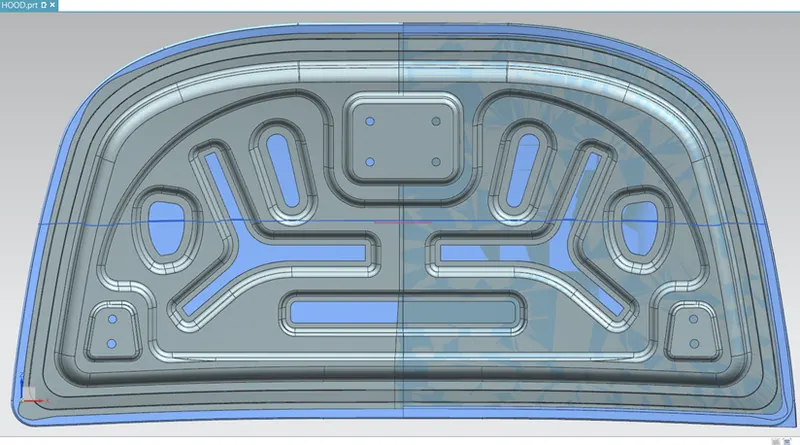
Main purose of the inner hood is to provide the strength,rigidity to the outer panel, mounting components wil be fixed to the inner panel also to minimise the reaction force passing to the pedestrian during crash by undergoing the deformation by collision. It is formed using the above mentioned sheet metal process lie deep drawing, embossing. it is provided with the uniform thickness of 0.75mm and attachment places with the reinforced thickness of 1.5mm.
Reinforcements are provided based on the FEA analysis carried out in iterations to improve the strength
Hinge
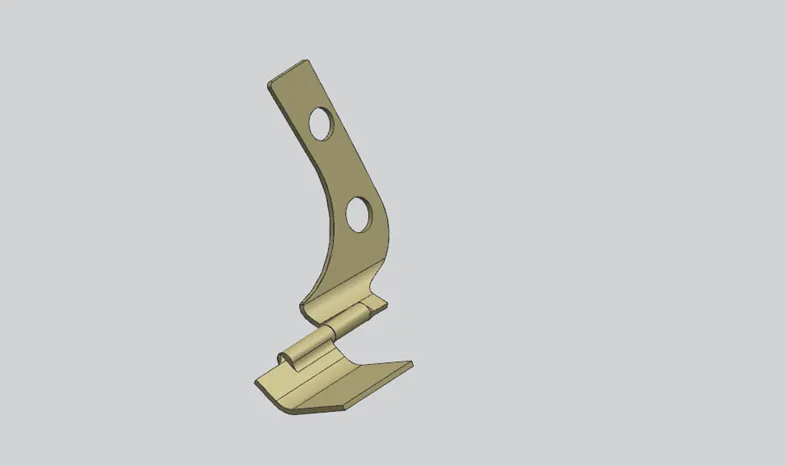
Hinge is a mounting component which fixes the hood with the fender. The latch must be fixed perpendicular to the hinge axis so that the hood opens or closes properly.
Striker
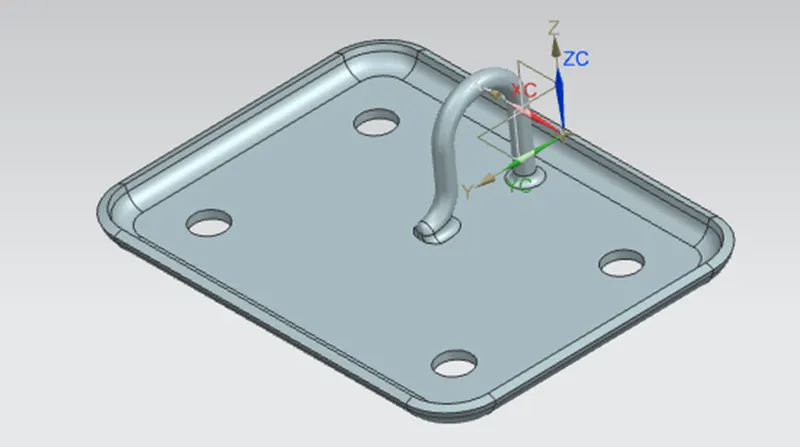
Striker is also called as latch , its function is to ensure hood is securely locked and doesnot open up by itself unless the pedestrian opened it with the manual lock release or with the actuators.
Assembly
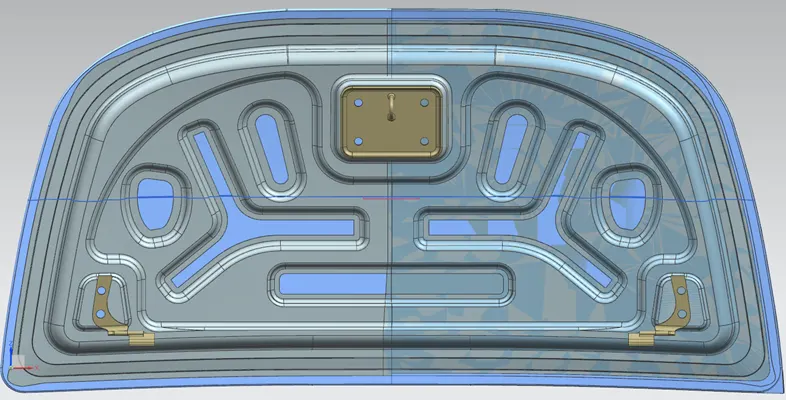
Inner hood is fixed with support and outer hood sheet is covered over it by the process of hemming or seaming. Hemming is carried with different rooler pasing over it from different angle and cariied out in step by step process like bending, pre hemmng, hemming, verifing. seaming is similar to hemming but additionally we connect the ends with the glue seam materials
Latch Trajectory
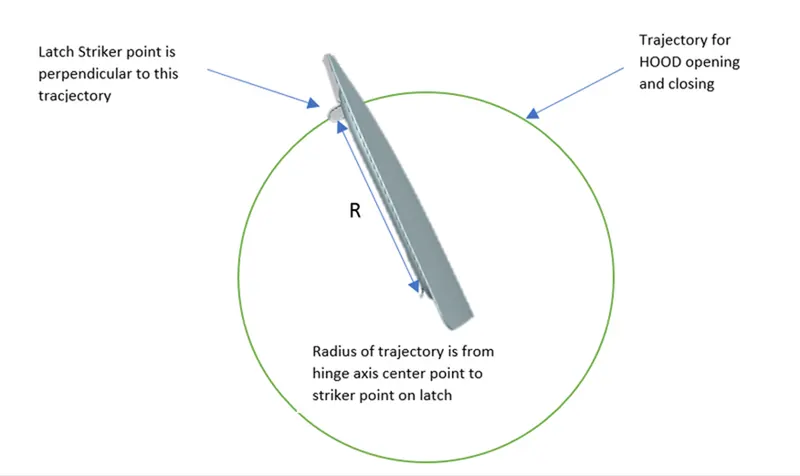
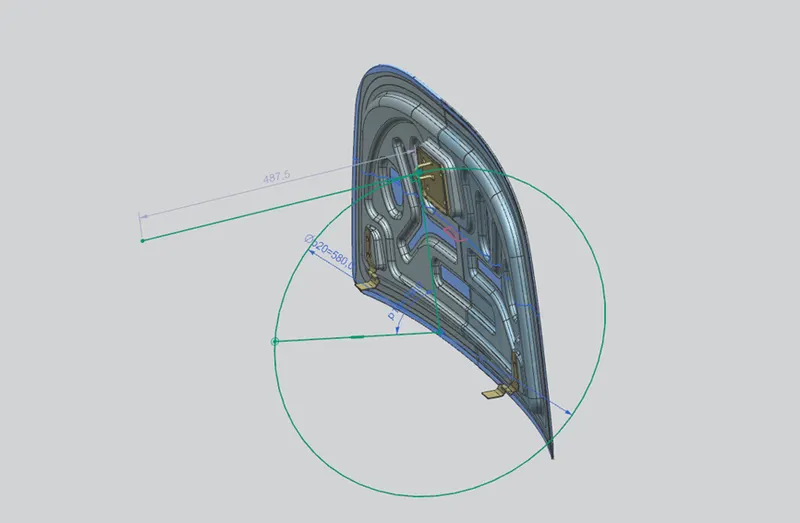
Latch Trajectory is the formed by circle drawn from the hinge axis to the striker line of axis is matched perfectly.
Latch trajectory is for aligning the striker in the perfect manner based on the hinge axis , so while opening or closing the latch will follow the trajectory and move uniformly in the position and orientation to provide smooth opening and closing with the least tension or compressive force.
Hemming
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
Mastic data
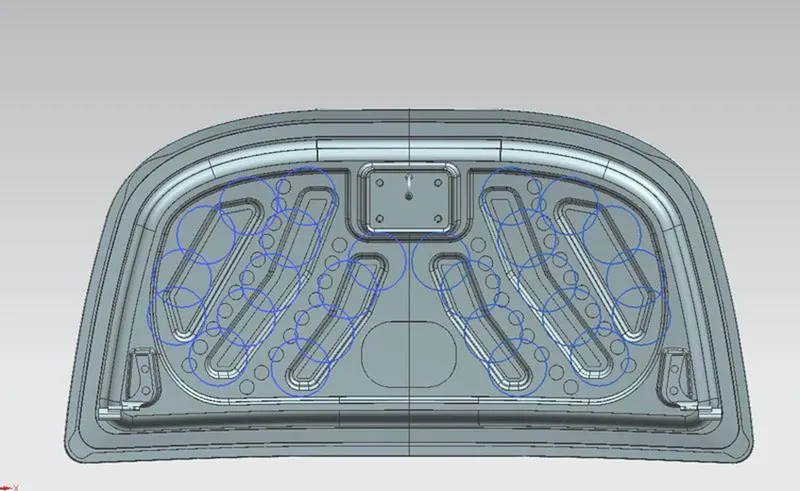
A mastic is the sealant which gets hardened when exposed to heat. It is used as hood support between outer panel and inner panel. Basic functions is to fills a gap between two or more sublayers, provide sealing property throughout the service life time of sealant, provide physical barrier to the adhesion of substrate.
example : sample mastic image
Thus the design is carried out based on the requirements and also considering the manufacturing feasibility of the components.