Hood design-Week 2
HOOD ASSEMBLY CHALLANGE
OBJECTIVE
To develop the hood inner and outer panels considering the safety, functionality and manufacturability, following the industrial standards.
ABSTRACT
Body in white (BIW) is the stage in automobile manufacturing in which a car body's frame has been joined together, that is before painting and before the motor, chassis sub-assemblies, or trim (glass, door locks/handles, seats, upholstery, electronics, etc.) have been integrated into the structure. Assembly involves different techniques such as welding (spot, MIG/MAG), riveting, clinching, bonding and laser brazing. In car design, the "body in white" phase is where the final contours of the car body are worked out, in preparation for the ordering of the expensive production stamping die. Extensive computer simulations of crash-worthiness, manufacturability, and automotive aerodynamics are required before a clay model from the design studio can be converted into a body in white ready for production.
Body in white (BIW)
The hood (North American English) or bonnet (Commonwealth English) is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment, or trunk (boot in Commonwealth English) on rear-engine and some mid-engine vehicles, for maintenance and repair. Hoods are typically made out of the same Material as the rest of the body work. This may include steel, aluminium, fiberglass or carbon fibre. However, some aftermarket companies produce replacements for steel hoods in fiberglass or carbon fibre to make the vehicle lighter. Hood consists of an outer panel and an inner panel. The inner panel provides strength and support, where the outer panel is a metal cover which have styling factors.
HOOD – TYPES
There are two major types of hoods
- Inlaid hood
- Wrap around hood
- Inlaid hood
It is lightest among all types of hoods. But it is easily subjected to border defects and body unevenness during manufacturing. Here the design done is INLAID HOOD
- Wrap around hood
As name itself it wrap around the car body. It can mask the geometrical defects and provide adequate stiffness. It is relatively safer than other types as it provides more safer areas for the pedestrian during impact.
Hood - Design requirements:
- Pedestrian safety
- Occupant safety
- Vehicle quality
- Styling
- Ability to manufacture
1. Pedestrian safety
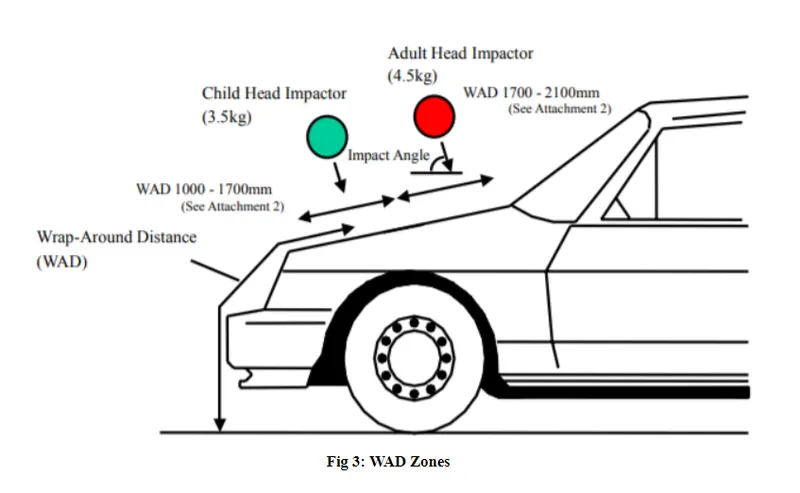
Vehicle designers usually focus on understanding the car-pedestrian interaction, which is characterized by the following sequence of events: the vehicle bumper first contacts the lower limbs of the pedestrian, the leading edge of the hood hits the upper thigh or pelvis, and the head and upper torso are struck by the top surface of the hood and/or windshield. Most pedestrian deaths occur due to the traumatic brain injury resulting from the hard impact of the head against the stiff hood or windshield. In addition, although usually non-fatal, injuries to the lower limb (usually to the knee joint and long bones) are the most common cause of disabilities. The hood of most vehicles is usually fabricated from sheet metal, which is a compliant energy absorbing structure which poses a comparatively small threat. Most serious head injuries occur when there is insufficient clearance between the hood and the stiff underlying engine components. A gap of approximately 10 cm is usually enough to allow the pedestrian’s head to have a controlled deceleration and a significantly reduced risk of death. Most limb injuries occur due to a direct blow from the bumper and the leading edge of the hood. Wrap Around Distance (WAD) is the distance from the ground level to the end of the hood as shown in the image.
- Occupant safety
The hood panels should be designed in such a way that it diverge the impact forces during a collision away from the occupants inside the cabin. The forces should be damped properly to avoid or reduce the risk of injuries and death.
- Vehicle quality
Here the factors such as torsional stiffness, dent resistance, corrosion resistance, weight distribution, and noise attenuation etc. are considered.
4. Styling
It is a major factor that often influence the vehicle sales in the market. The outer panel is the main consideration here as it is the only component that is visible outside. The factors such as surface quality, tight radii on hemmed panel edges aesthetic design etc. are crucial factors. Other than styling, aerodynamic factors are important while designing the outer panel.
- Ability to manufacture
Here various sheet metal operations such as blanking, piercing, embossing, hemming etc are used for manufacturing the hood components. Minimum 7 degree draft angle is maintained respective to the tooling direction considering the stamping process. Mastic points were implemented to join the outer and inner panels as we cannot apply spot welding process here. The materials used are typically steel or aluminium based.
Various manufacturing processes are as follows;
Blanking is a metal fabricating process, in which a metal workpiece is removed from the primary metal strip or sheet when it is punched. The material that is removed is used as new metal workpiece or blank.
Piercing is a shearing process. Here raw metal is pierced with a machining tool, resulting in the creation of a circular or other shaped hole.
Sheet metal embossing is a stamping process for producing raised or sunken designs or relief in sheet metal.
Hemming is the process in which the edge is rolled onto itself. Hems are commonly used to reinforce an edge, hide burrs and rough edges, and improve appearance.
Here,
- Outer panel thickness = 0.75mm
- Inner panel thickness = 0.75mm
- Reinforcement thickness = 1.5mm
Design Methodology
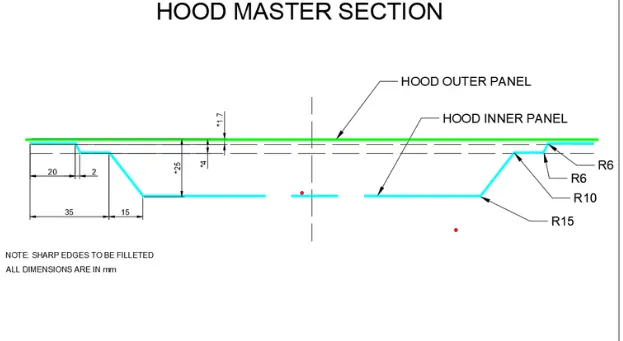
The master section of the hood inner panel is shown in the image below. It provides information such as distance between various layers (emboss), fillet radii, width, clearances etc.
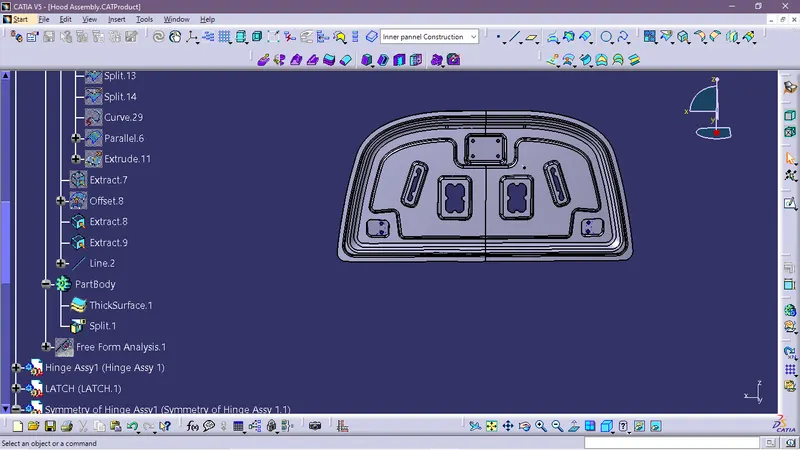
Hood inner panel was designed at first. The various stages of inner panel development are shown below. Here, the embossings were created. The main design consideration is to diverge any impact forces away from the passenger cabin.
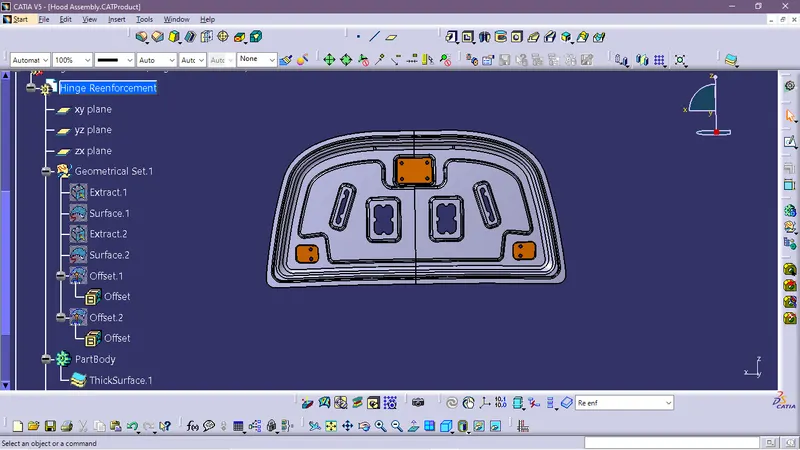
Necessary cuts were provided for sufficient deformation of the outer panel without any restrictions caused by the inner panel in case of pedestrian impact. This also helps to reduce the overall weight of the hood. Also mastic sealant points were created on the inner panel. Provisions for attaching the fixtures, various holes for supplying viper fluid and ED bath drain holes, hinge and striker attachment holes etc. were designed. Diabolo embosses for fixing the hinges and striker on the inner panel were also created as shown below.
Impact forces diverging away from the passenger cabin
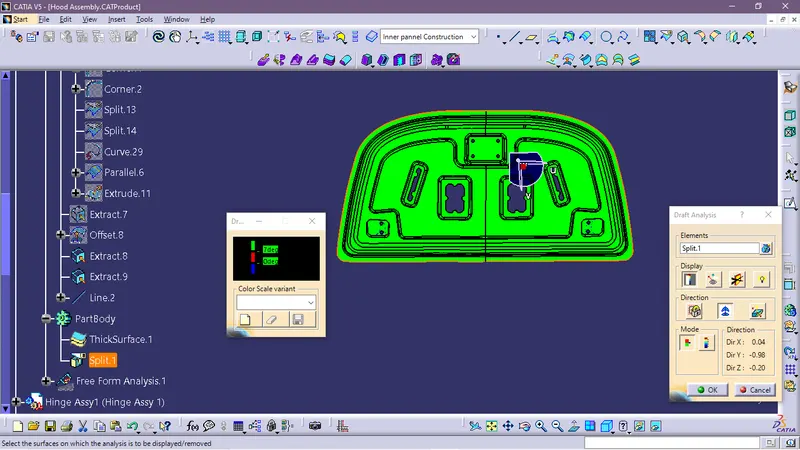
The draft analysis of the hood inner panel was successfully performed with a minimum angle of 7 degree with respect to the tooling direction.
Draft analysis
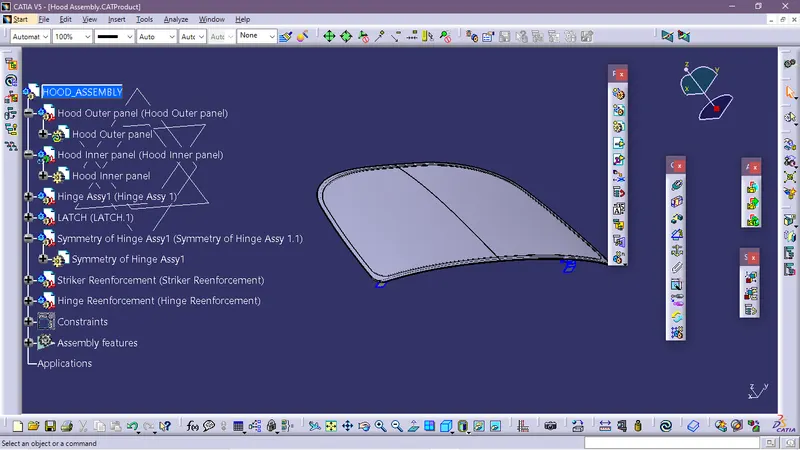
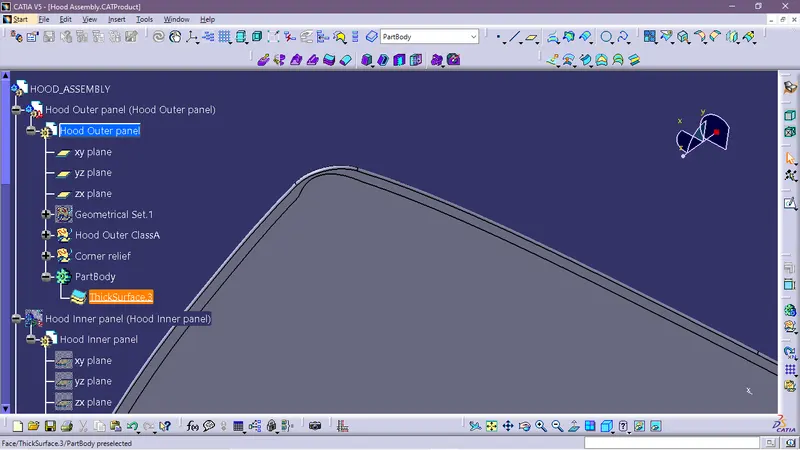
Development of the hood outer panel was the next step. Thickness of the sheet metal used is 0.75mm. The hood outer panel and inner panel have a clearance of about 5mm at mastic sealant application points. Hemming is a sheet metal working process in which the edges are rolled over onto itself. 0.2mm clearance provided between the surfaces of inner panel and hemmed edges of outer panel for application of structural adhesives. Necessary corner reliefs were also provided.
Outer panel of hood
Hinge and striker reinforcements
Hemming
Full assembly
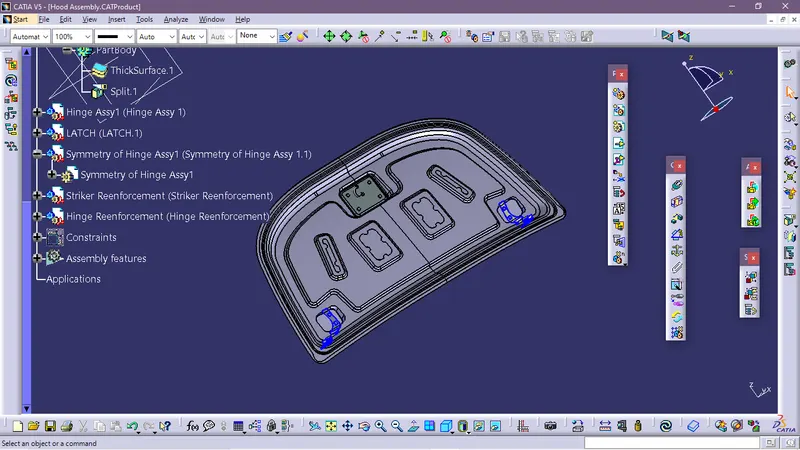
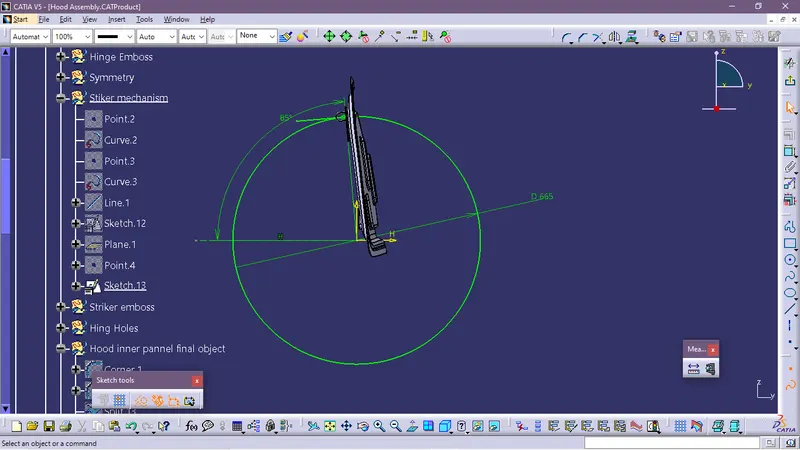
The striker is positioned in such a way that it’s tip perfectly follows the trajectory (cyan coloured circle) with hinge axis as centre. Then only the proper opening and closing of the hood can be performed.