Hood design-Week 2
Hood Consists of
- Outer panel
- Inner panel
- Stiffner pad
- Hinge Reinforcement
- Stricker Reinforcement
Factors considered while designing Hood
- NVH (Noise Vibration and Harness)
- Hinge Axis
- Gas stay requirement
- Latch and Stricker point
- Deformation Bracket
- Pedestrian Rating
- Euro Ncap regulations
DESIGN CONSIDERATIONS FOR CAR HOOD:
- Head clearance zone
- Consideration of Noise Vibration Harshness (NVH): Noise, vibration, and harshness (NVH), also known as noise and vibration (N&V), is the study and modification of the noise and vibration characteristics of vehicles, particularly cars and trucks. While noise and vibration can be readily measured, harshness is a subjective quality, and is measured either via "jury" evaluations, or with analytical tools that can provide results reflecting human subjective impressions.
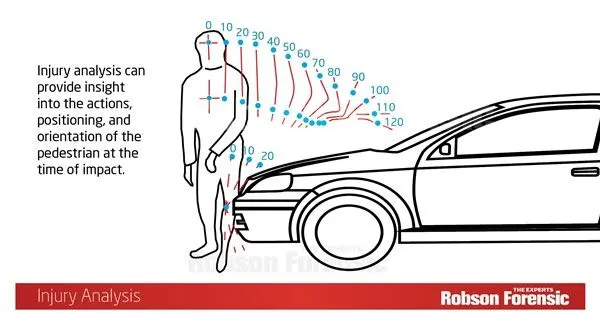
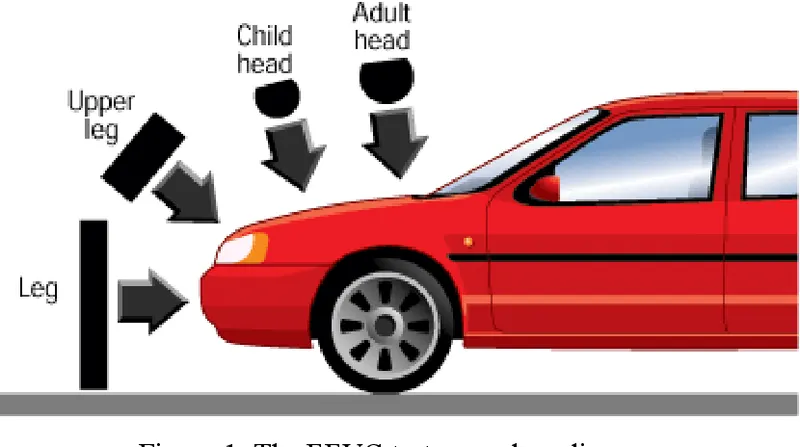
- Pedestrian safety: Pedestrian safety is important consideration while designing the hood. According to the wrap around distance and pedestrian head impact zone hood is designed. Safety is the most important criteria in automobile designs which concentrates on both pedestrian and occupant safety. The pedestrians are the most vulnerable road users and are at high risk of traffic accidents. The major reason for the fatality of the pedestrian in traffic accident is due to the head injury resulting from the hard impact of the head against the stiffer hood or the ground. This leads to the necessity of new inner hood panel which is less stiffer and pedestrian friendly. The area at the head impact zone is made softer to reduce the impact force during accident.
Design parameters
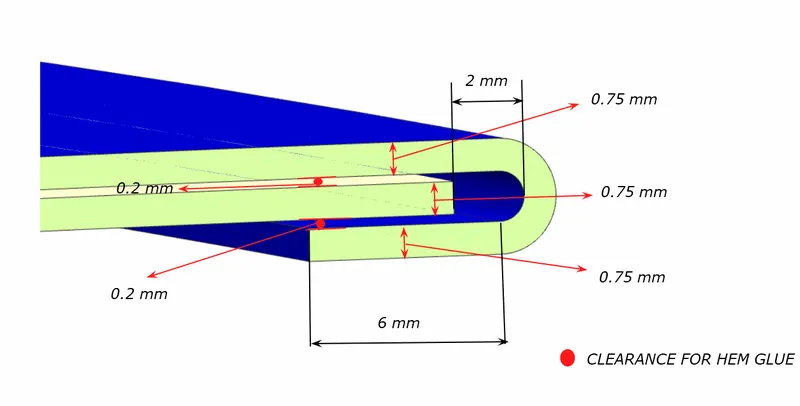
- Outer Panel Thickness = 0.75mm
- Inner Panel Thickness = 0.75mm
- Reinforcement Thickness = 1.5mm
Procedure:
Hood outer panel :
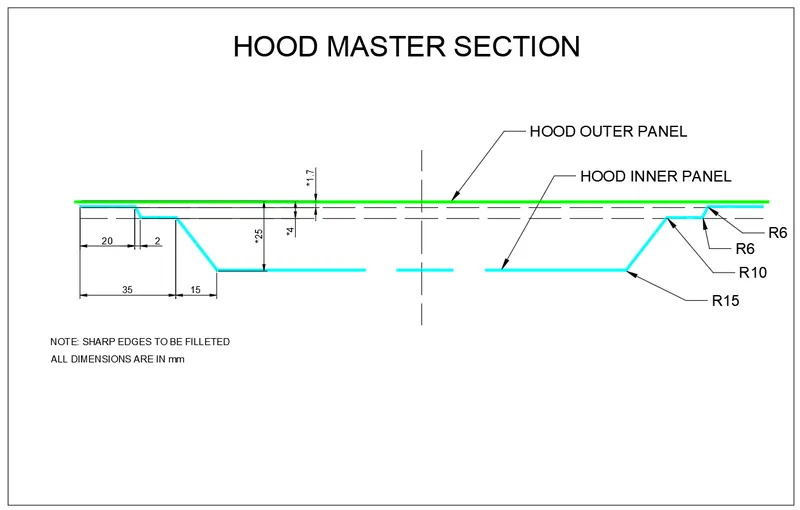
Outer panels are the aesthetic elements of a car. It is the styling team who provides the skin for the outer panel. The shape, position and size of the hood should satisfy the safety norms. So while designing the hood we should give more importance to pedestrian safety. The outer panel is attached to the inner panel by hemming. So, it is necessary to provide required hemming flange and reliefs for the hemming operation. We also provide mastic sealants between outer panel and inner panel to reduce vibration.
Hood inner panel :
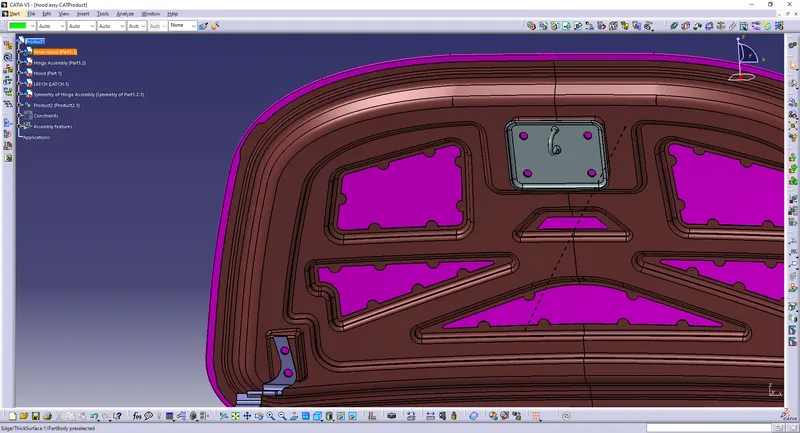
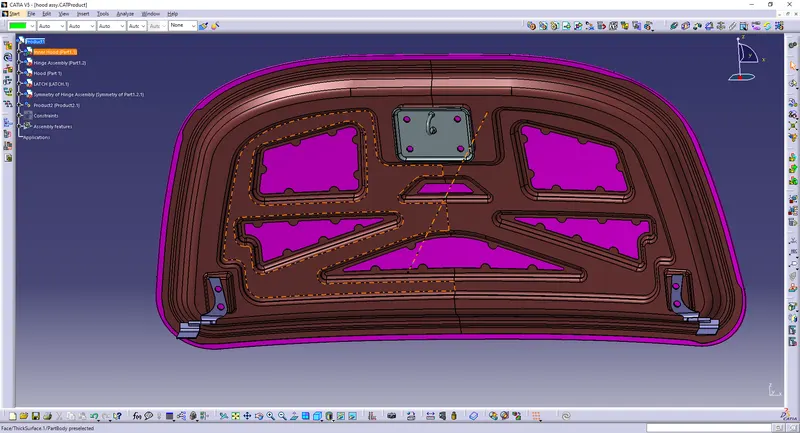
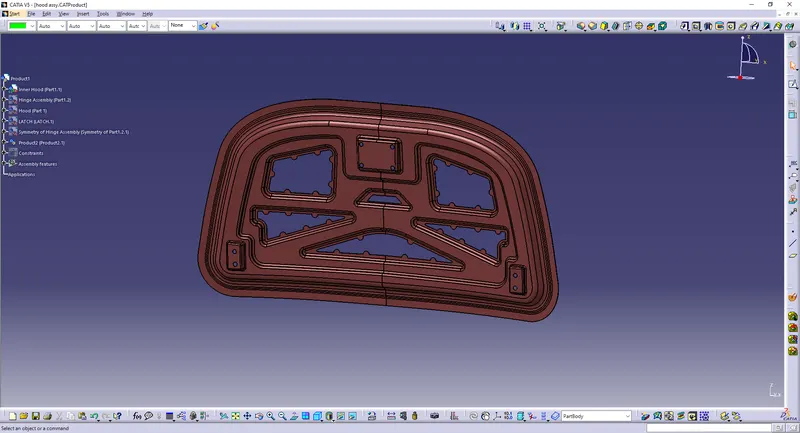
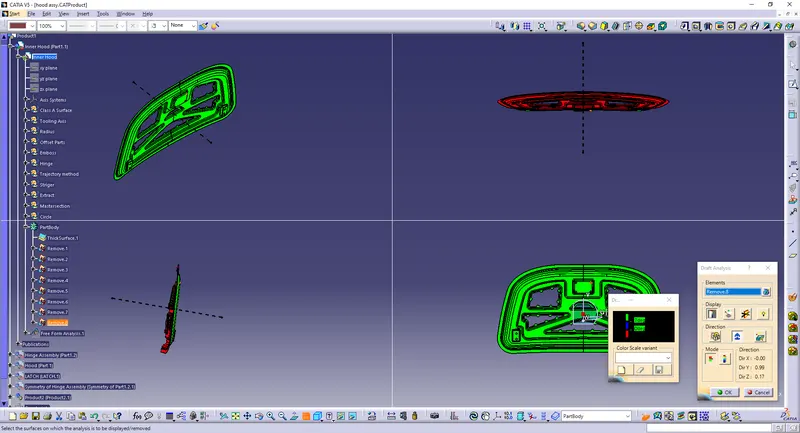
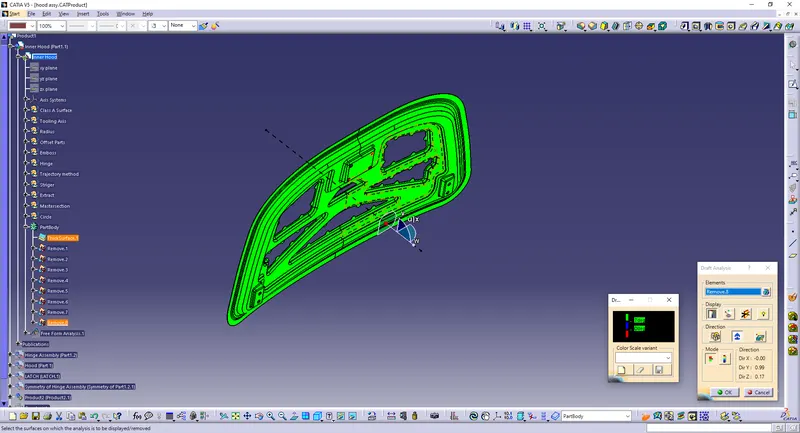
Inner panel is the part that gives strength and rigidity to the outer panel. The master section represents the initial emboss shape and size. Then we provide the emboss for the latch and hinge elements after fixing the location.
Reinforcement :
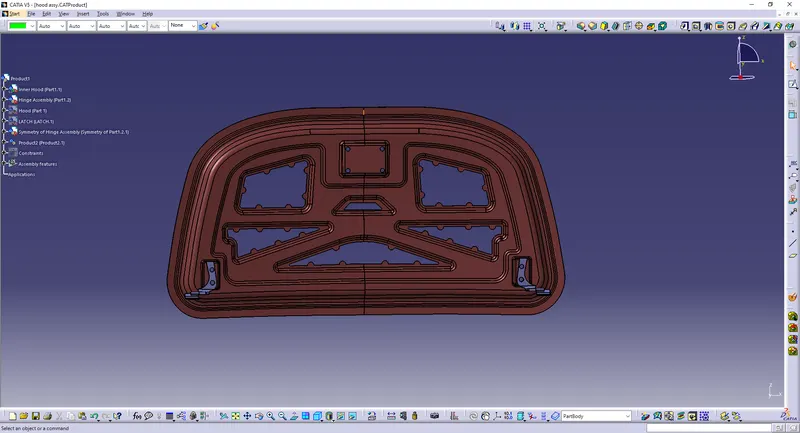
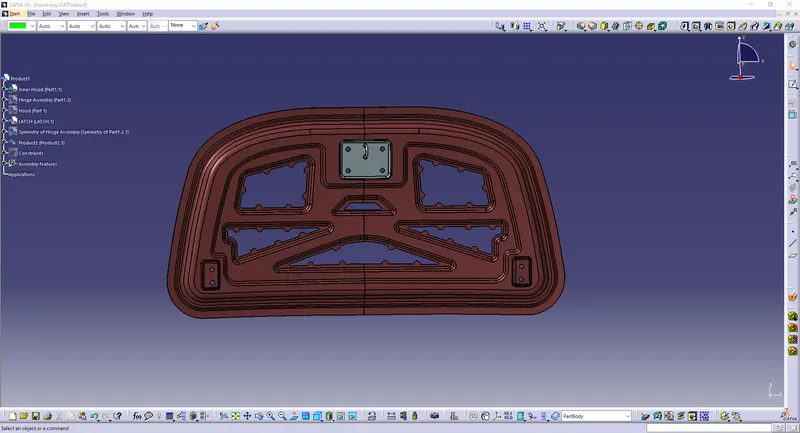
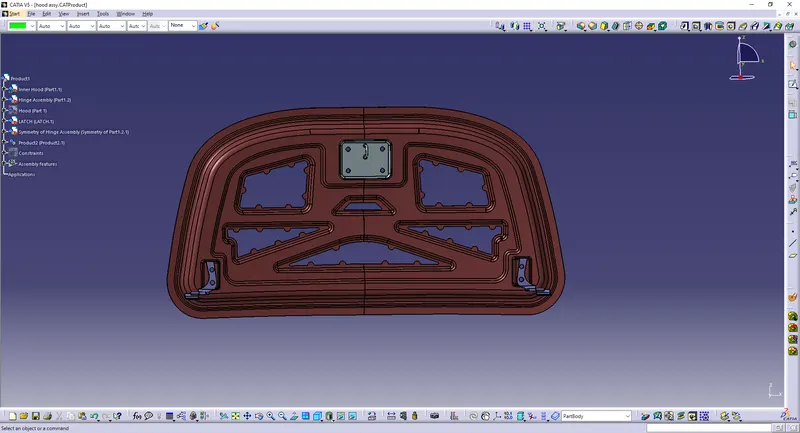
Reinforcements are provided according to the design requirements. Mainly it is provided at the hinge and latch regions to improve the strength locally. Usually thickness of reinforcements will be higher than that of the inner panels and the value varies according to cost and requirement. According to the design requirement here it is given 1.5mm thickness to both hinge and latch reinforcements.
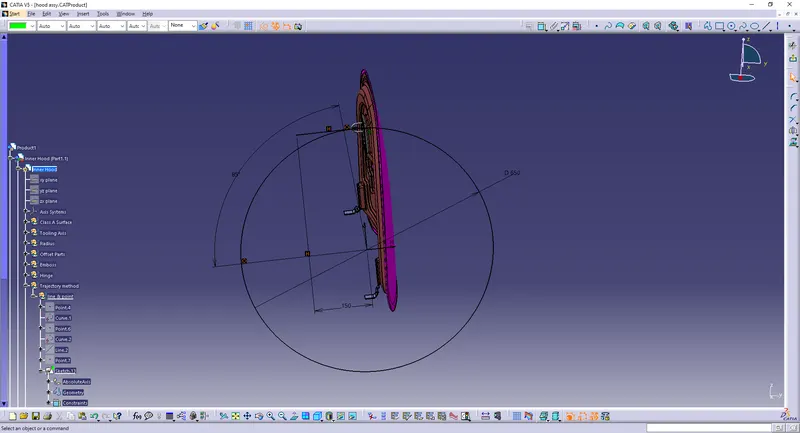
 Latch Trajectory :
Latch trajectory is given by the circle drawn from the hinge axis point. Hinge axis point is the centre point of the hinge axis. First, we can fix either the latch or the hinge. If we have fixed the hinge position then we should plot the Trajectory circle for the latch. For proper mating condition the striker axis through the tip of the striker should be tangential to the latch trajectory.
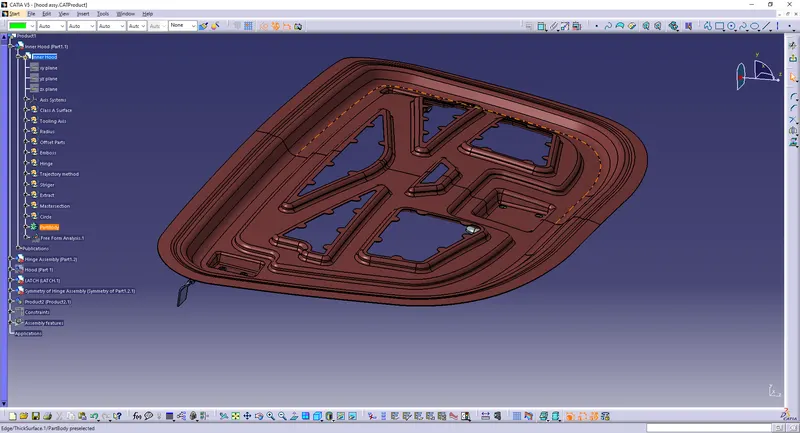
Emboss :
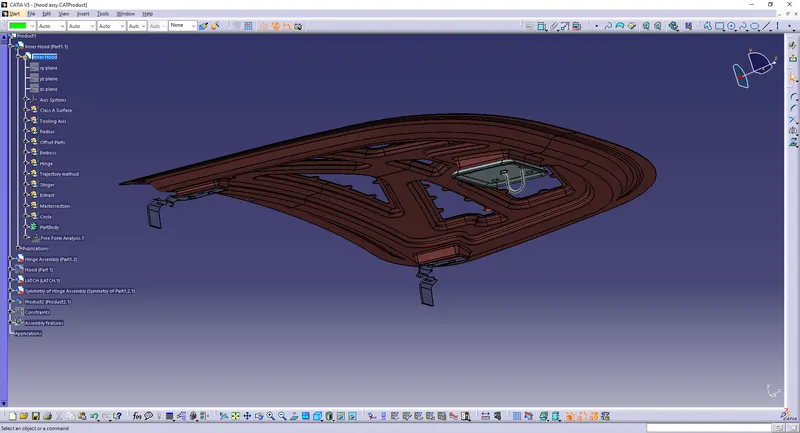
We provide different embosses throughout the inner panel . We can increase the stiffness of the inner panel through these embosses. The shape and size of the embosses also determines the direction of the force distribution resulted from frontal collision. The force should be always distributed away from the passengers. Here in the figure the embosses are designed in such a way that the force is directed to either sides of the car.
Mastic Sealant Data :
Hood commonly possess large surface area and hemming can only be provided through its boundary. We cannot use other joining techniques like welding, riveting etc because they leave marks on the outer panel which spoil its aesthetic appearance. So, mastic sealants are used to stick the inner surfaces of outer panel and inner panel. Mastic sealants are elastic compound that behave like rubber. It is applied between the inner and outer panels at specified spots. Each spot of mastic sealants has its effect around a circular region of 80mm diameter. Thus, the mastic points are arranged in such a way that it covers the areas away from the hemming which are more vulnerable to vibrate.
Hemming :
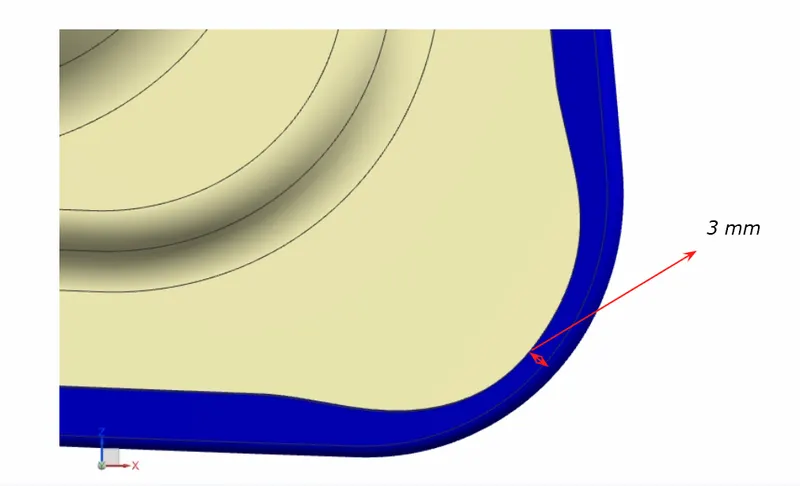
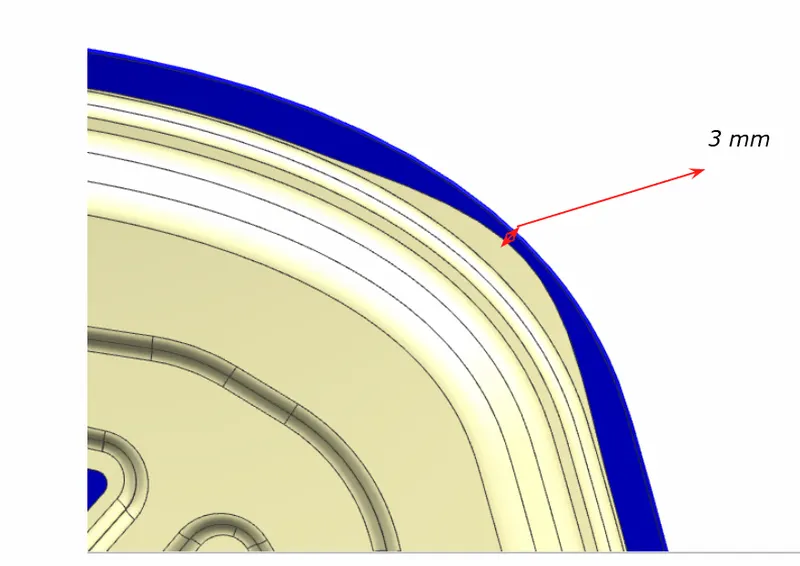
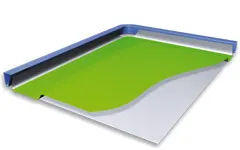
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders. The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, overlaps in the corner areas or material roll-in. It is important to provide required reliefs at the corners.
There are two types of hemming operations:
Conventional die hemming
Conventional die hemming is suitable for mass production. In die hemming, the flange is folded over the entire length with a hemming tool. Normally the actual hemming is a result of a forming operation in which the flange is formed with a hemming tool after the drawing and trimming operations have been completed. The formed flange is then hemmed in several process steps. These steps include, for example, the pre-hemming and final hemming depending on the respective opening angle of the flange. Production plants for conventional die hemming are very expensive, but the cycle times are very low.
Roll hemming
Roll hemming is carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller which follows a defined path.
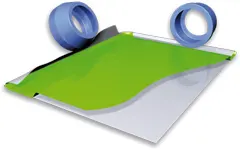
The accuracy of the hemming operation is very important since it affects the surface appearance and surface quality of the component. Material deformations, which occur during the hemming process, can lead to dimensional deviations and other typical hemming defects, including splits and wrinkles in the flange, material overlaps in the corner areas and material roll-in. To address these important issues, AutoForm Engineering offers the enhanced version of AutoForm-HemPlannerplus, which allows for the efficient planning of hemming process.
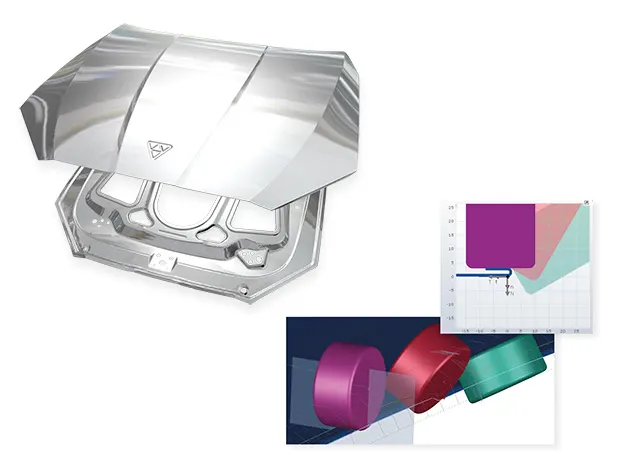
AutoForm-HemPlannerplus, which is now fully integrated in AutoFormplus R6, enables users to easily define and optimize the hemming operation. In combination with AutoForm-Solverplus, this software offers immediate benefits, such as: efficient planning of hemming processes to meet quality and cost requirements, effective implementation for early feasibility and final validation studies, rapid identification of typical hemming defects, prediction of full assembly springback after hemming as well as easy data exchange internally between different departments and externally between OEMs and suppliers. In addition, this software allows for compensation of inner and outer parts as well as any adjustments of the hemming equipment.
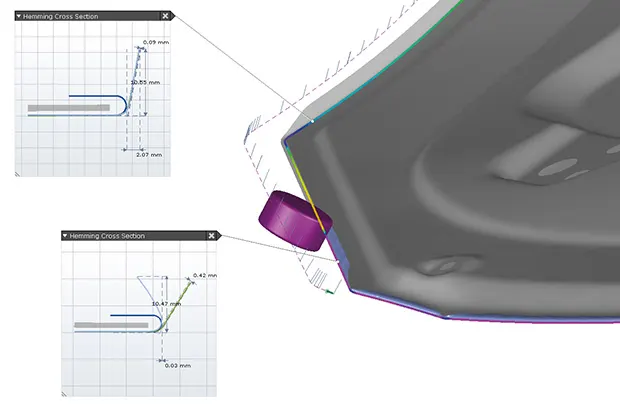
AutoForm-HemPlannerplus supports roll, conventional die and table top hemming. Depending on the product development process phase, the software supports two use cases, namely quick and advanced hemming. Quick hemming is used in the early stages of product development and production planning when the die layout of the drawing and forming operations is still not available. Advanced hemming is used in process engineering when the detailed definition of the forming operations is already available.
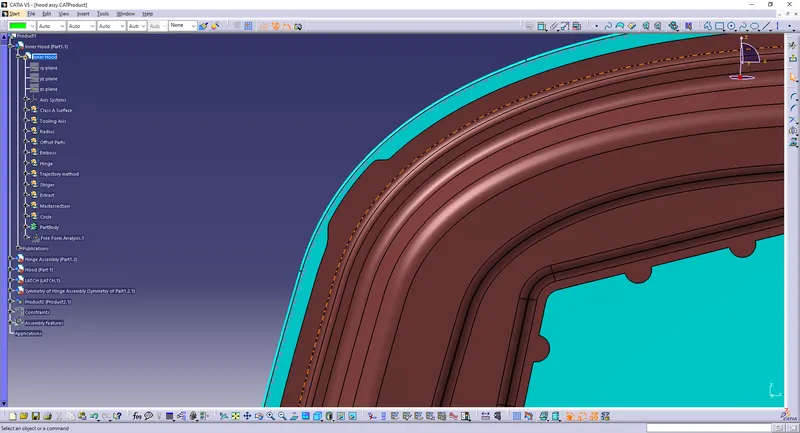
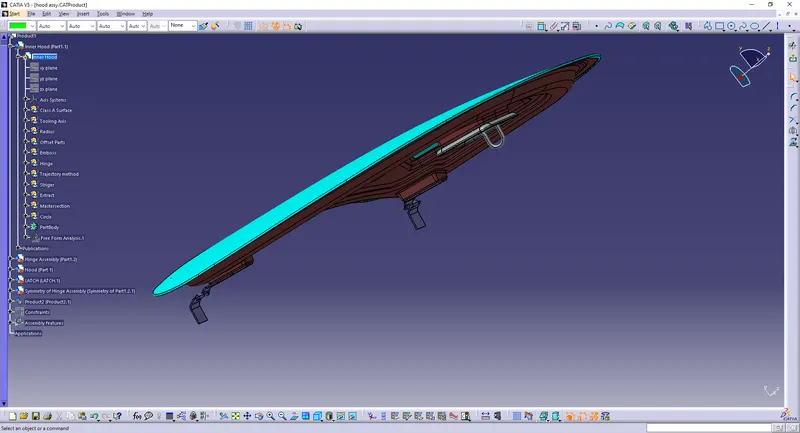
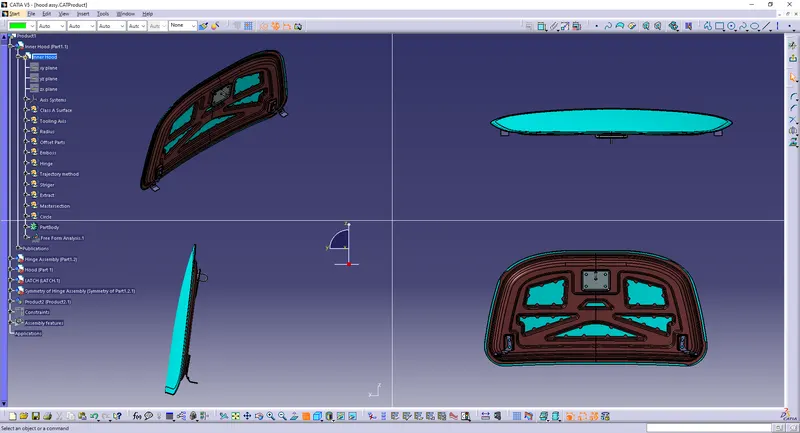
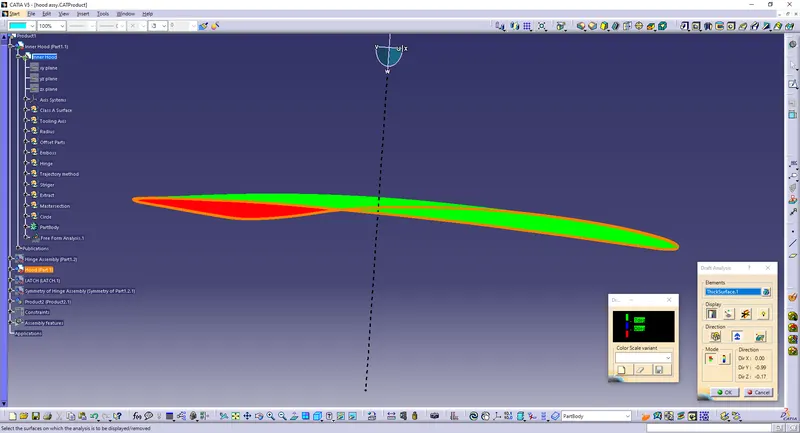
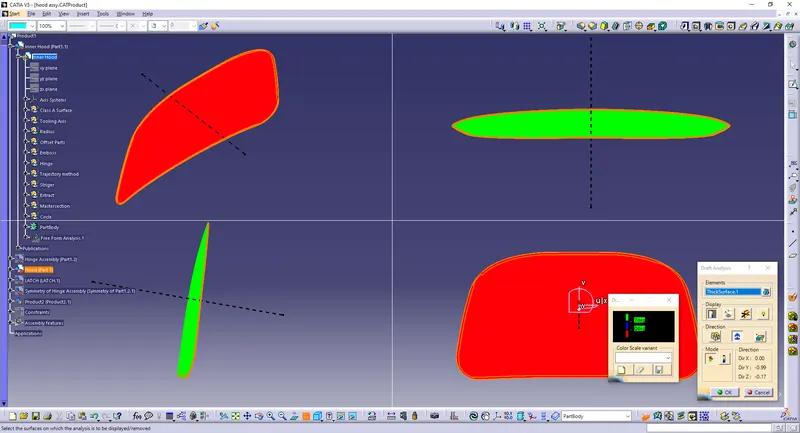
Final Assembly
Conclusion
In this challenge I learned to design the hood inner panel, outer panel with the help of master sketch and the styling surface. And also learnt the assembly of Hood inner panel, Outer panel, and the reinforcements like latch and hinge assembly.