Week 8 - Challenge 1 - Base Bracket Design
Base Bracket Design
AIM:
To Create the Solid part body of BASE BRACKET from given Class-A surface
OBJECTIVE:
The objective of this challenge is to create BASE BRACKET DESIGN along with Solid Part Body from Class-A surface following OEM design standards in CATIA SURFACE WORKBENCH and PART DESIGN.
BASE BRACKET DESIGN:
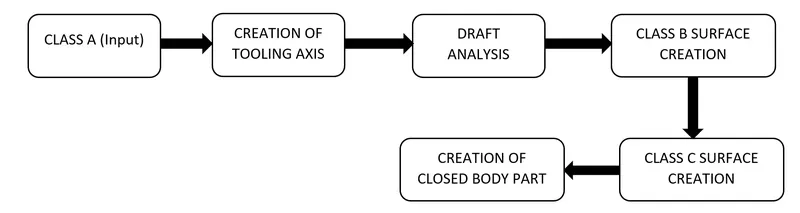
Procedure to be followed:
MATERIAL:
Duroplast is a distinctly 20th-Century material that's sort of a cross between Bakelite and fiberglass. Like the former, it's a thermosetting plastic, and like the latter, it's reinforced with fibers (cotton or wool, in this case).
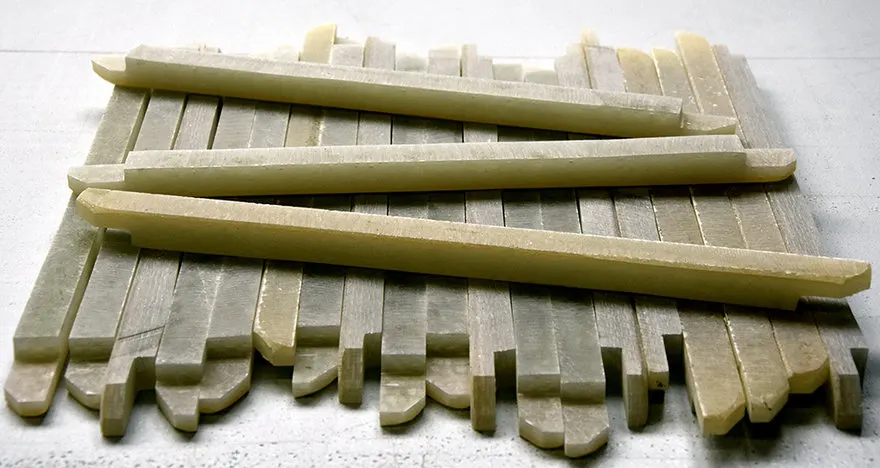
From a production standpoint, Duroplast was attractive because it was lightweight, relatively strong, and could easily be shaped into compound curves using presses, as with auto body panels made from more expensive steel. Additionally, the fibers used to reinforce Duroplast could be produced from cotton waste.
For producing high-volume durable goods like cars, metal was always the first choice for mid-20th-Century industrial powerhouses like the U.S. and the U.K. More resource-poor countries like East Germany, however, had to make do with Duroplast for the bodies, saving the metal for the chassis and mechanicals. Thus the Trabant, the East German car manufactured from 1957 until the country's collapse, had a steel chassis but a Duroplast body.
DESCRIPTION:
Four stages of design life cycle are as follows:
- Concept sketch: These are the imaginative and innovative sketches. Concept sketches can be defined as collection of visual cues sufficient to suggest the design to an informed observer. These are the basic sketches which provides general idea about design of the product. These sketches are provided to system either in 2D or isometric form. Example, concept sketch of an automobile.
- Class A Creation: Class A surface refers to those surfaces which are VISIBLE and abide to the physical meaning, in a product. For styling-class A surfaces of automobile ALIAS software is used. These class-A surfaces are used as an input for an Automotive Plastic Designers
- CLAY MODELING: In clay modeling class-A surfaces are provided to clay modeler who design actual model of automobile using industrial clay. Class-A surfaces and clay models are co-related. Using clay modeling physical representation of design is possible which helps in further modifications in the design of the vehicle. Clay modeling of an automobile is most common example of a clay modeling.
- NPD CAD: New Product Development (NPD) Computer Aided Drafting (CAD). This process involves forming strategy, organizing requirements, generating concepts, creating product.
CLASS A SURFACE:
Class ‘A’ surfaces are primarily used in the automotive environment and refer to those surfaces which are visible in a product. In other words: A - class surfaces are those aesthetic/free-form surfaces, which are visible to us , and have an optimal aesthetic shape and high surface quality.Here, one should understand the difference between the internal or external and visible or hidden surface. The surfaces or regions which are visible nowadays are considered for Class-A modelling. It is one of the reasons why the importance of Class-A modelling is increasing day by day. Majority of the time this term is used in Plastic Part designs.
INPUT CLASS-A SURFACE:
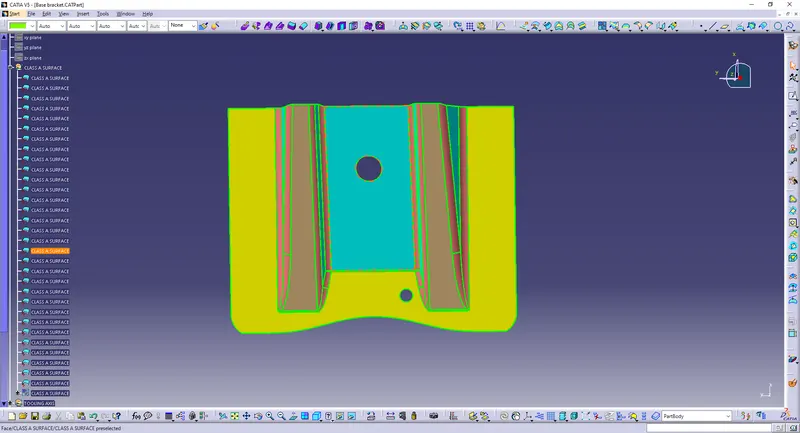
Base Of Class A Surface .
Class A Tree Strucure
FIRST STEP TO JOINT THE CLASS A SUFACE:
Joint the class A surface by using the joint icon in catia v5. The jointed fig. is given below.
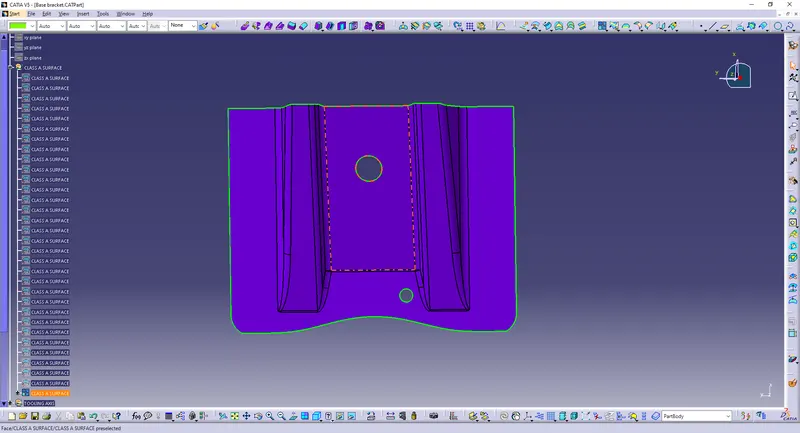
Class A Surface Has Been Jointed
TOOLING AXIS CREATION:
Class-A surface is first analyzed to create tooling axis or tooling direction that molds pull apart in injection molding. Tooling direction is vital for plastic product design as it decides direction for mold separation.
Steps followed for creation of tooling axis:
- Reference point is first created on extracted surface.
- New axis system is deployed to plot clearance lines.
- The X direction and Y direction along the class A were used to create tooling axis
- Two clearing lines were bisected to form Tooling axis.
- Graphic properties of tooling axis were change before publishing.
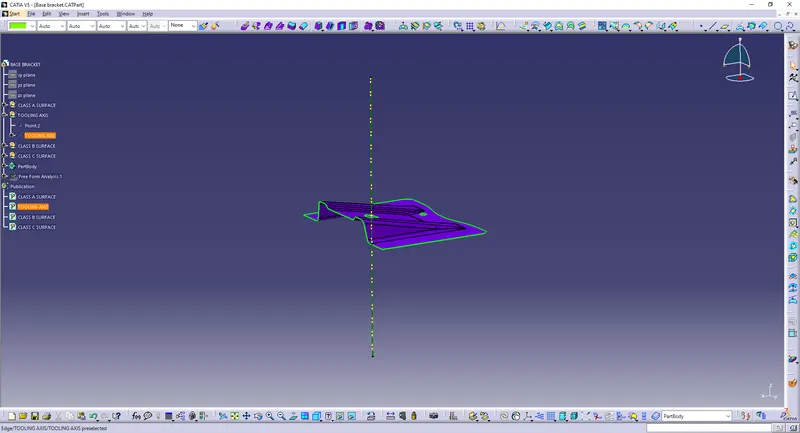
Tool Axis Has Created
DRAFT ANALYSIS:
Draft Angle: The draft angle is the amount of taper for molded or cast parts perpendicular to the parting line. It can be measured in degrees or mm/mm (in/in). As plastic cools, it shrinks and therefore shrinks onto molding surfaces. Because of this and a few other reasons, we draft (angle) the walls of the plastic part, so as the part is removed it breaks free from the molding surfaces easier and without dragging. A functional part for injection molding has to have drafts facing both cavity and core sides to reduce the risk of damage to the parts and ensure ejection. What’s also important is to overcome the vacuum forces by letting air in between the metal and the plastic for the part to release properly. Adding an adequate draft angle ensures that warpage upon ejection is prevented while maintaining a decent cosmetic finish.
- Draft angles are generally a requirement of injection molding design (though there are a select few soft materials, like nylon, that can get away with draft angles of zero).
- Draft should be a part of design for manufacture, and Plastic Product Designer should be aware of its need at the outset of the design process. This allows considerations for design requirements to be taken into account.
Nominal Values for Draft angle:
- 3 Degrees is nominal Draft.
- 5 Degrees can also be manufactured. But it will increase the manufacturing cost.
- 7 Degrees for textured surface.
Importance of DRAFT in Injection Molding:
- Reduces the chance of damage to the part due to friction during release
- Reduces wear and tear and chances of damage to the mold
- Ensures a uniform, smooth, unscratched finish when required
- Ensures the integrity and uniformity of other surface finishes and textures
- Reduces overall cooling time by lessening or eliminating the need for unconventional ejection setups
- Most, if not all, of these benefits offer either direct or indirect overall production cost reductions.
Steps followed for Draft Analysis:
- The part created has to be changed to material mode in display frame.
- Compass is enabled. Align compass along with tooling direction.
- Lock command is then applied to fix compass along with tooling axis
- Color codes are classified and Draft angle is applied.
- Running point analysis is used to display permissible draft angle.
DRAFT ANALYSIS REPORT:
DRAFT ANALYSIS ON CLASS-A SURFACE:
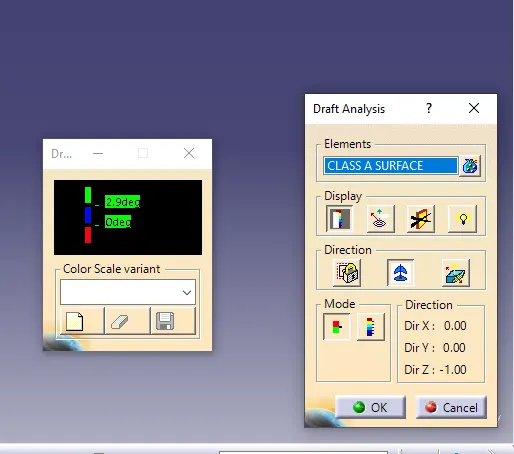
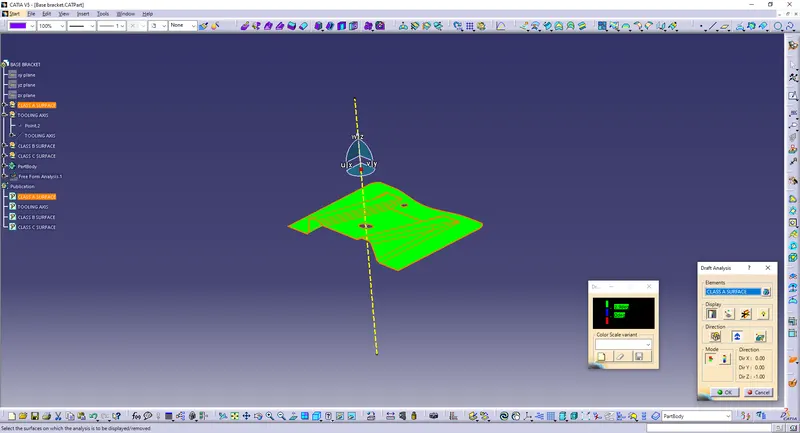
Drafting Take Place In The Img.
CLASS B SURFACE:
The Class B finish is a quality finish with only minimal imperfections. A Class B finish is the most common finish for exterior surfaces. It is normally specified on surfaces such as external covers, panels, and parts that are fairly prominent.
Step 4:Class B Surface Creation:
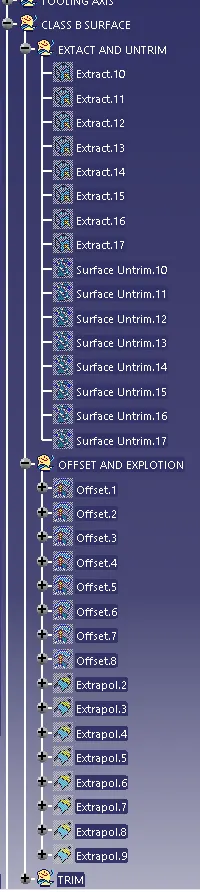
- Extract the relevant surfaces from Class-A surface which excludes the Fillets and holes. One example of extract is shown in the Figure 13
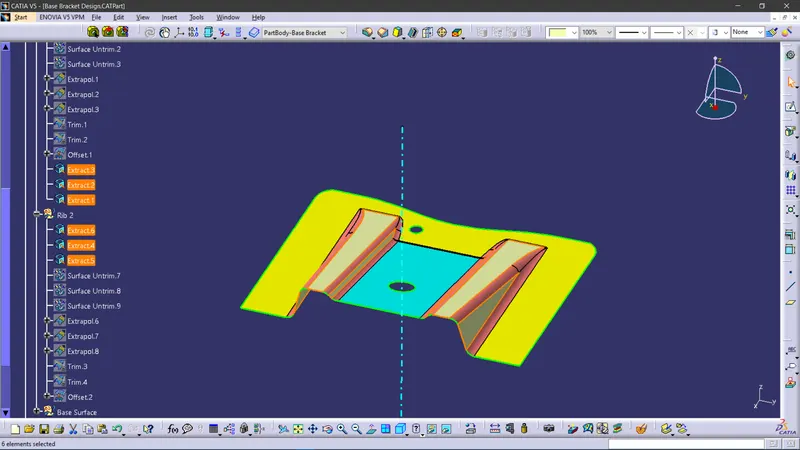
Extract of surfaces from Class A.
- Use Untrim Command to untrim the surfaces and create a natural extend.
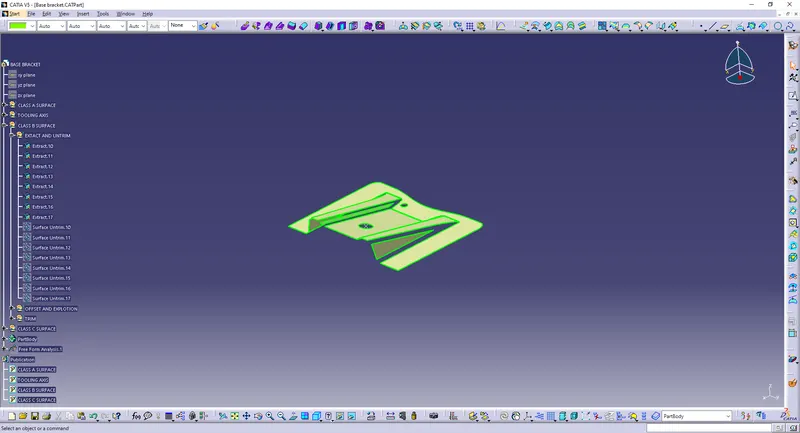 Untrim of Extracted Surfaces.
- Extrapolate the untrimmed surfaces so that each of them intersects clearly and pass way forward than the Class A which will help in its trimming in further operations.
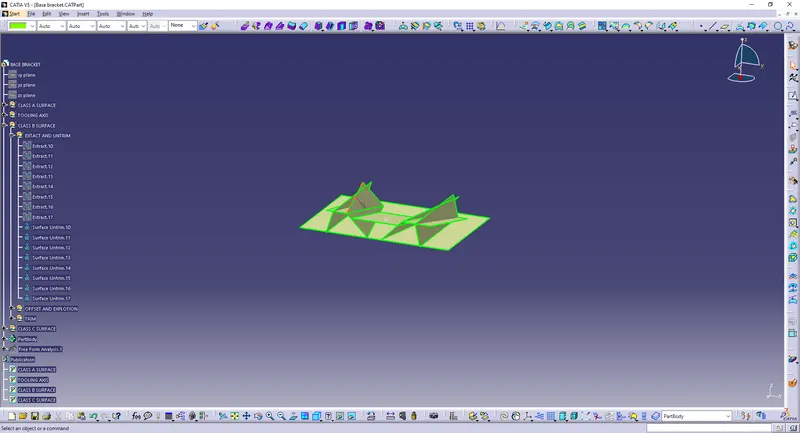
Extrapolated Surfaces created from Untrimmed Surfaces.
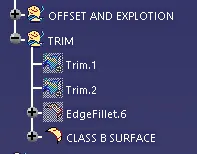
- Trim the extra surfaces to obtain similar extended surfaces as in Class A.
- The operation performed on the Ribs of the Bracket.
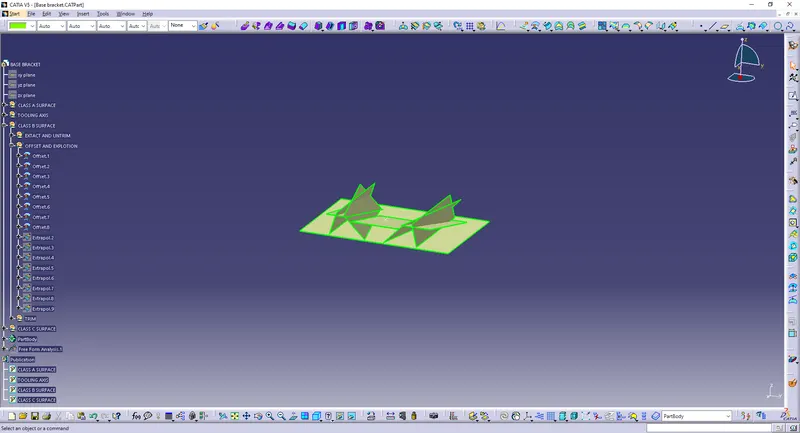
Trimming of Extrapolated Surfaces.
- Offset the obtained Trim to the value of required Thickness of the Part. In this case of Bracket, the thickness value is 2.5 mm.
- The offset faces are the part of B-Surface.
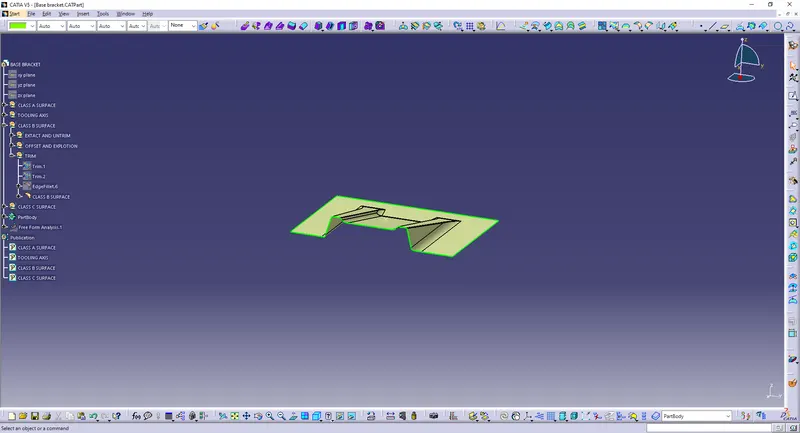
Offset highlighted showing the start of B surface creation.
- Do The Similar operations namely : Extract, Untrim, Extrapolate, Trim, Offset for the other faces from the Class A excluding the Fillets.
- Trim the extra surfaces such that it crates similar surface as Class A.
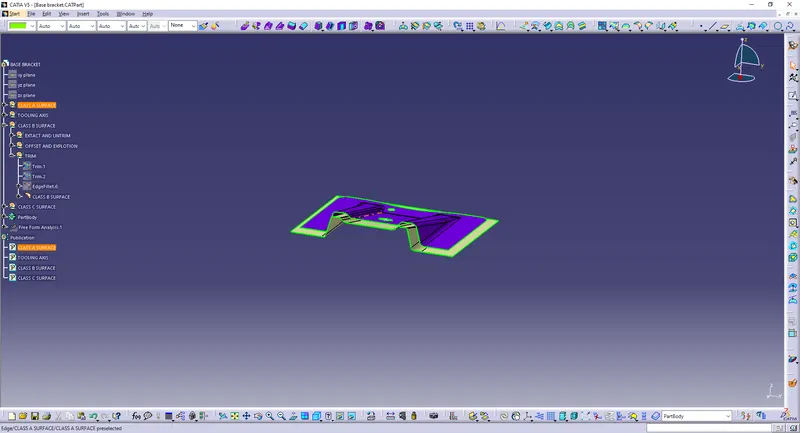 Output after trimming extra surfaces.
- Create Fillets while maintaining the part thickness between the Class A and Class b surfaces.
- The Value of Fillet is given by the equation (B surface fillet = A surface fillet + - Thickness of the Part).
- The sign + or – must be decided so as to maintain the part thickness which in this case is 2.5mm.
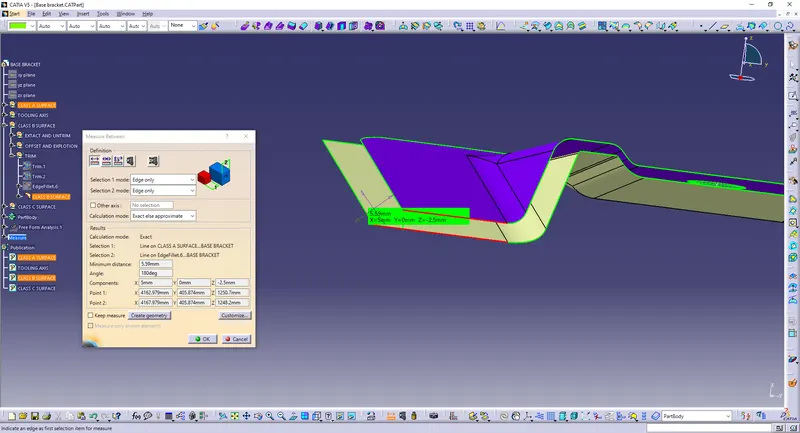 Fillets to be created as per the Part Thickness (in this case 2.5mm).
- The fillet values can also be obtained by maintaining the thickness in the intersection sketch of the two surfaces.
Class B surface of Base Bracket highlighted in Blue.
CLASS C SURFACE:
The Class C finish allows more imperfections than Class A or B. Class C is often specified for interior surfaces not readily visible, surfaces that will be covered by another part when assembled, or surfaces which the Customer feels do not need to meet a high cosmetic finish. This Class is generally used for parts or surfaces which are not viewed after installation or viewed only for service.
Step 5: Class C Surface Creation:
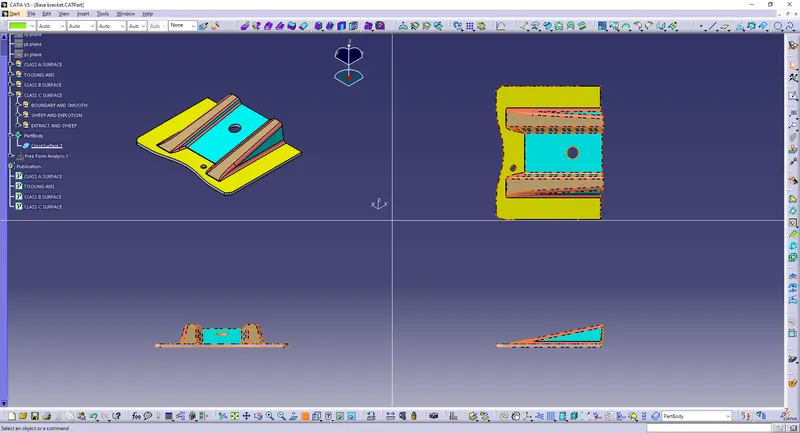
- Use Boundary option to extract the outer boundary of the Class A surface
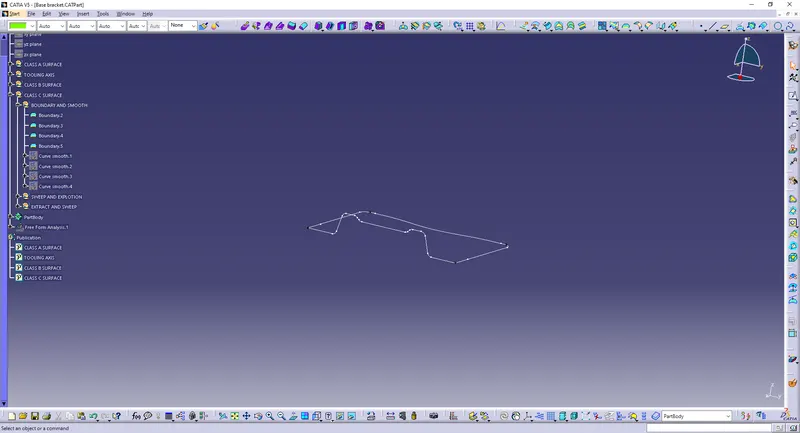
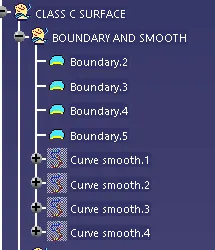
Extracted Boundary from Class A.
- Use Sweep Operation to extrude the boundary using the Draft direction option and selecting the Tooling Axis as the direction.
- Use draft angle as 3º and Sweep it well beyond the B surface.
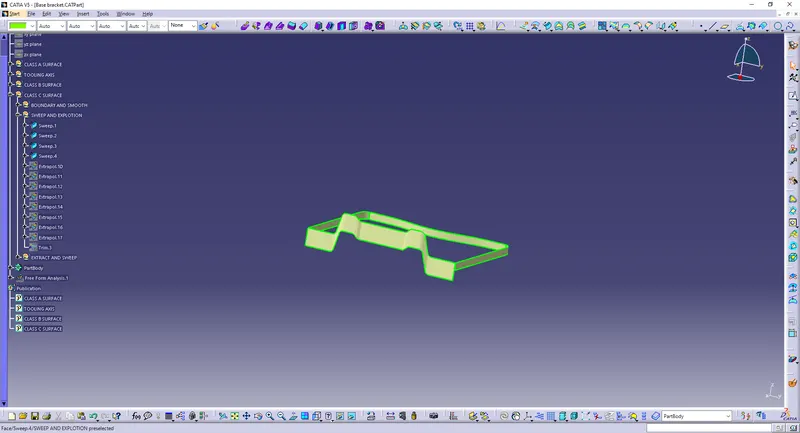
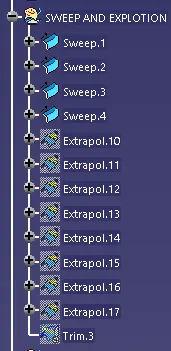
Sweep operation with draft direction and draft angle.
- Use similar options of Boundary extract and Sweep for the holes on Class A.
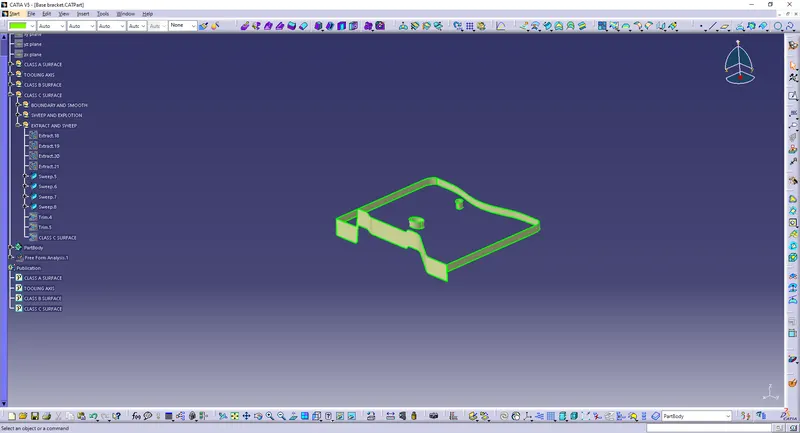 Sweep operation for remaining Class C surfaces .
- Join all the Swept surfaces along with the Class A Surface.
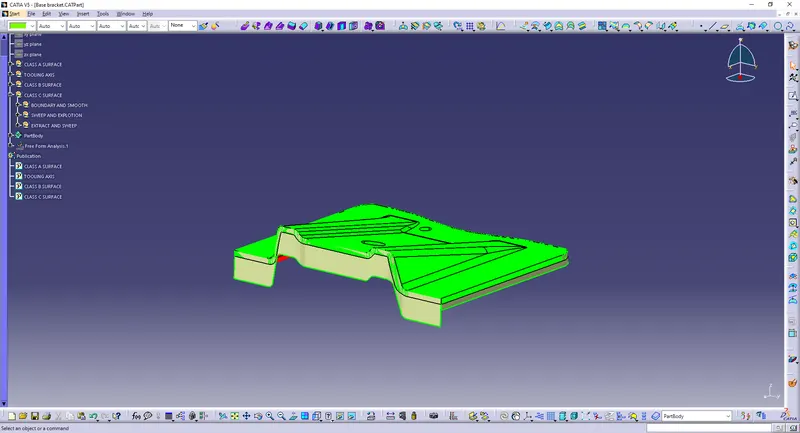 Join Operation between Class A and Class C surfaces.
- Trim the obtained Joined surfaces with the Class B surface to obtain the final enclosed Surface for the Bracket.
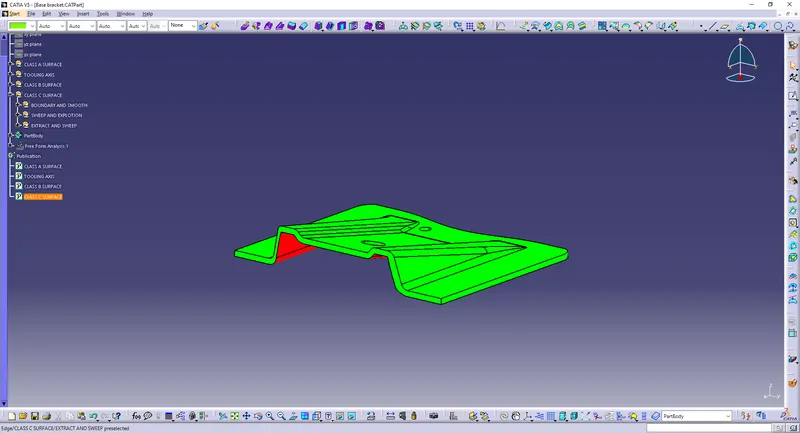
Final Closed Surface.
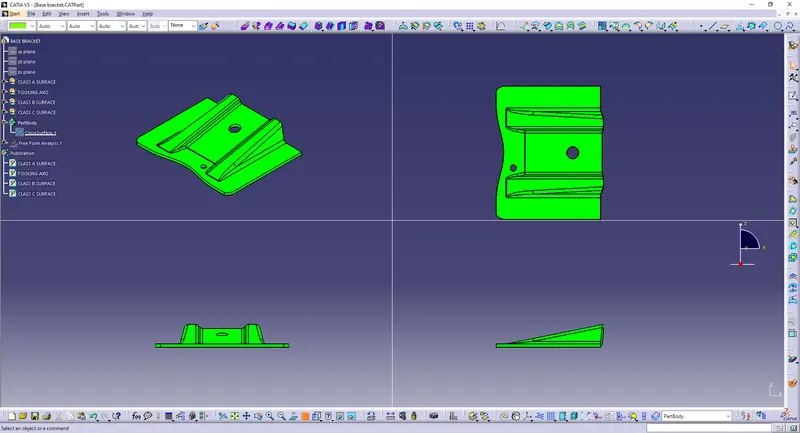
- Switch to Part Design Workbench and use Closed Surface option to create a Solid Part from the final obtained surfaces.
- The part created is the required Base Bracket designed from a Class A.
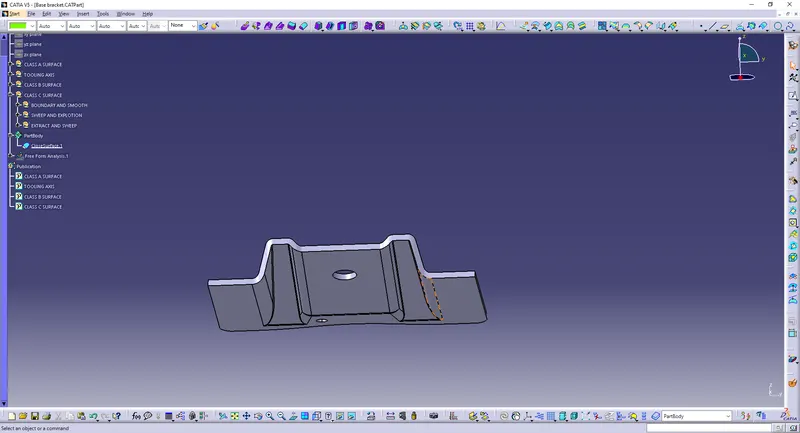
Final Closed Surface converted to Solid Part.
Conclusion:
The Design of Plastic Component - Base Bracket from Class A is completed using concepts of Draft angle, Draft Analysis, Tooling Axis, Class B and Class C creation and converting Closed surface to a solid part.
BASE BRACKET (FINAL SOLID BODY):