Week 8 - Challenge 4 - Bumper
AIM:
Create the Bumper Plastic component through the given Class-A surface. To begin with, the tooling axis for the given Class-A Surface should be created meeting the requirements of the draft angle and at the end perform the Draft analysis on the model.
Take the Thickness of the component to be 3 mm.
OBJECTIVE
Conduct a Draft Analysis for the Bumper Plastic by determining the appropriate Tooling Axis and check if all the features are above the Nominal Drafting.
CLASS A SURFACE:
In automotive design, a class A surface is any of a set of freeform surfaces of high efficiency and quality. Although, strictly, it is nothing more than saying the surfaces have curvature and tangency alignment – to ideal aesthetical reflection quality, many people interpret class A surfaces to have G2 (or even G3) curvature continuity to one another.
CALSS B SURFACE:Class B surfaces are the secondary surfaces that you can see sometimes, but are less important, such as the inside of your glovebox, ash tray, etc.. These must be smooth and "error-free" as well, but are not held to the standards that class A surfaces are.
CLASS C SURFACE:Class C surfaces are the backside surfaces that can have tool marks, flash and other imperfections without hurting appearance, function, etc.
CREATED CLASS A SURFACE:
Class A Surface is all ready created by the designer, there are shown below as an image.
Steps followed
The class A surface is checked for the connectivity of the surface and ensure it is completely joined and there will be no gap between the surfaces.
If it is not join together make it with a minimum tolerance of 0.001 to 0.003 and check for connectivity of the surface.
Connectivity of the surface can be done by two ways by join method and by boundary method.
Split the surfaces into multiple profiles then Identify the surface where it is not possible to create a tooling axis and check on which direction is best fit for tooling axis and then define the tooling axis and draft direction.
Here for defining the tooling axis first we have created a point at middle of the base surface and create an axis with respect to that point then define the tooling axis using the intersect method by creating a bisecting line.
Then do a draft analysis on the class A surface and identify the draft angle then give the nominal value for the draft. 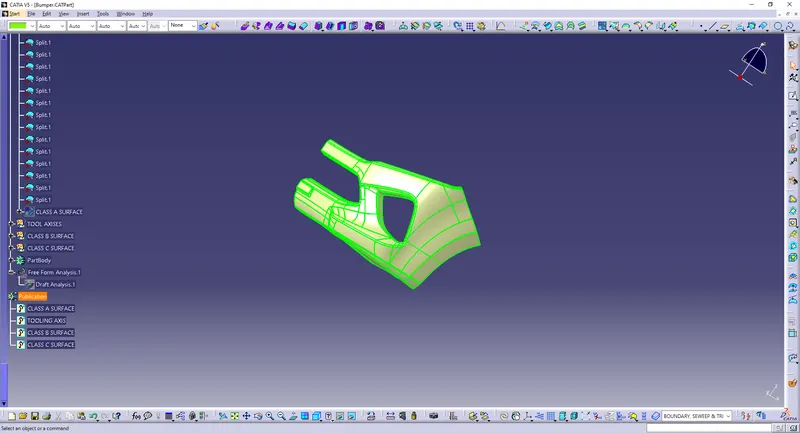 Fig.1.
fig. 2 & 3.
JOINT TOOL:
Using the joint tool just joint the Class A Surface after that extract tool is used for to create a tool axis if the selected surface as show in fig 4.
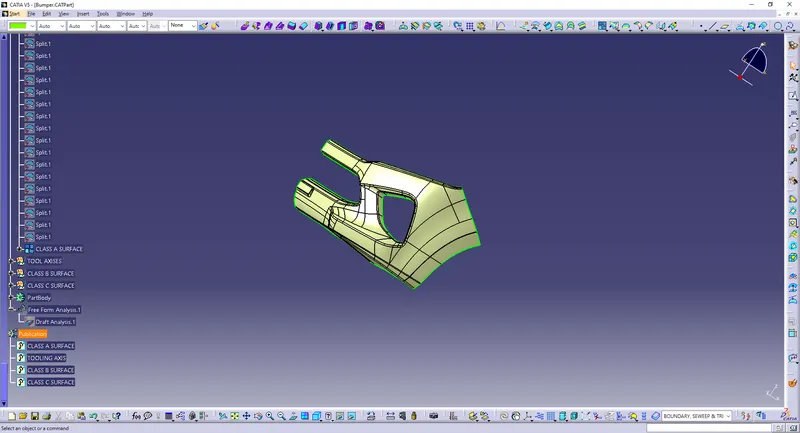
Fig.4
Tooling Axises:
Class-A surface is first analyzed to create tooling axis or tooling direction that molds pull apart in injection molding. Tooling direction is vital for plastic product design as it decides direction for mold separation.
Steps followed for creation of tooling axis:
- Reference point is first created on extracted surface.
- New axis system is deployed to plot clearance lines.
- The X direction and Y direction along the class A were used to create tooling axis
- Two clearing lines were bisected to form Tooling axis.
- Graphic properties of tooling axis were change before publishing.
- Show in fig. 5, 6, & 7
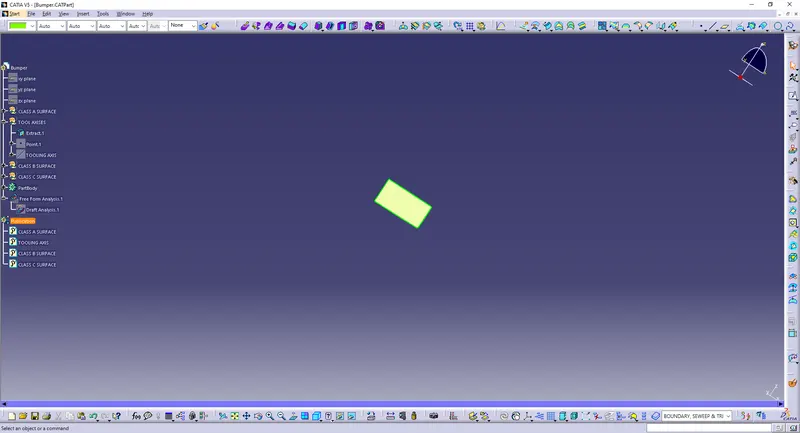 Fig 5.
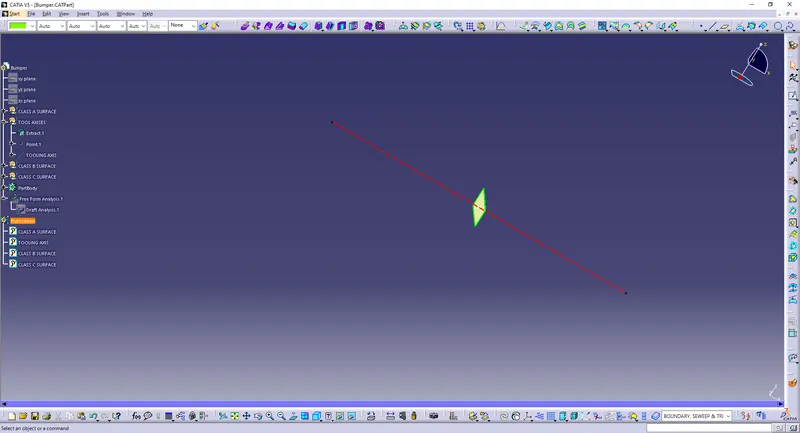 Fig 6.
Fig 7.
Tooling axis creation:
The direction in which the mould open and closes is called the tooling axis direction.
Check the connectivity of the surface and ensure there will be no gap between the surfaces and then define the tooling axis.
While creating a tooling axis please ensure to give the tooling axis on a flat length surface or the surface which have a hole on it.
Create a point on the middle of the base surface by using point on the surface command then create a intersection for the surface and extract the reference lines which will be helpful for creating the dummy tooling axis using the intersect method by creating a bisecting line..
Use the line command and draw the lines which is aligned with the extracted lines and extended it to the required length.
Bisecting method:
Identify on which plane we have to do more operations and create the plane or axis on the component area define it on the dummy tooling axis direction.
Intersect the class A surface with that plane then we will get a intersection sketch. Look for the profile (inclined line) which will create a problem and extract it then extending it by using line command.
Then create a bisecting lines with reference to the lines we have extended and this will be our main tooling axis.
In this case we have created tooling axis along with Y direction with reference to the base surface.
Draft analysis:
Draft allows for the component to release from the mould, most parts or applications require a minimum of 0.5 to 1 degree draft angle and 3 dgree draft angle is widely used as per the norm.
Change the material mode to customize mode before moving to the draft analysis.
Insert –analysis-feature draft analysis
Defining the draft direction Select draft analysis from the tool bar and click on the compass symbol and pull the compass from the right side top corner of the workbench and place it on the component where want to do the draft analysis. ‘W’ of the compass and tooling axis should be aligned on the same line.
Once the compass is aligned with the tooling axis click on the lock symbol and drag on the surface we will get a wrong mark then select that point a table will appear it shows the draft value on the table we can adjust the draft value and analysis it for all the edges and surfaces.
By clicking the on the surface and using the flipping tool we can assign the Flipping direction, the color of the surface change as per the flipping direction .
Analysis under running point and move the mouse on the surface and it will show the details of the surface deg direct at each and every point of the surface.
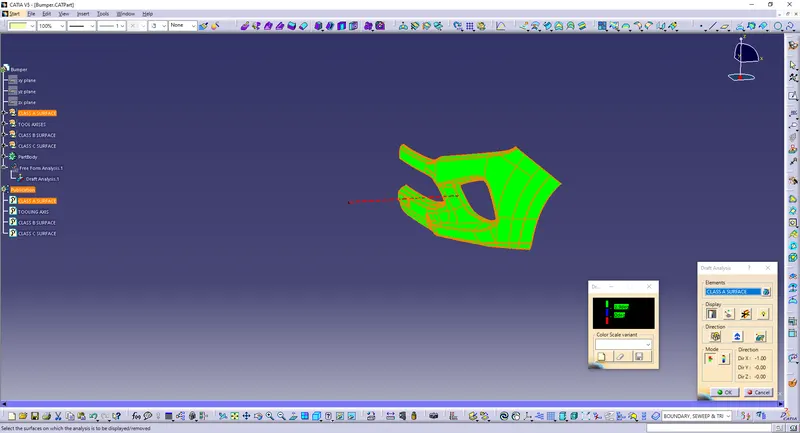
Fig. 7.1.
Class B Surface:
In the case of Class A the surface below is called core and the surface above is called cavity.
Class A is an aesthetics surface and class B is an engineering surface.
B surface should be inside the class A surface.
B surface can be divided into four surfaces the side walls, top walls, outer flange and the base surface and later trim them altogether.
First step is to create the side wall surfaces by extracting the required surface from Class A and untrimmed it thus we will get a single surface which will be extrapolated to get the required size and finally offset it to the inner side of class A as per the thickness of the material and trim them together and apply the required fillet by measuring the values from class A.
Base surface of the component is then extract, untrimmed, extrapolated, offset and trimmed.
The top walls can be directly extrapolated from the extracted surfaces and offset it for the required size of the material.
Then join the base, side wall and top wall by trim operations.
As the Outer flange is surface complex it can be divided into two parts and extract them then go for extrapolation, offset, split and join operations and finally check the for the connectivity by intersecting method.
Now all the four geometries are trimmed together to get the B surface.
Fillet is applied to the required surfaces by measuring the fillet value from the class A surface.
The Class B Surface creation are given below as IMG. :
STEP 1:
To create the below stracture we of to offset from the Class A Surface with the 3mm. The base is created are show below. 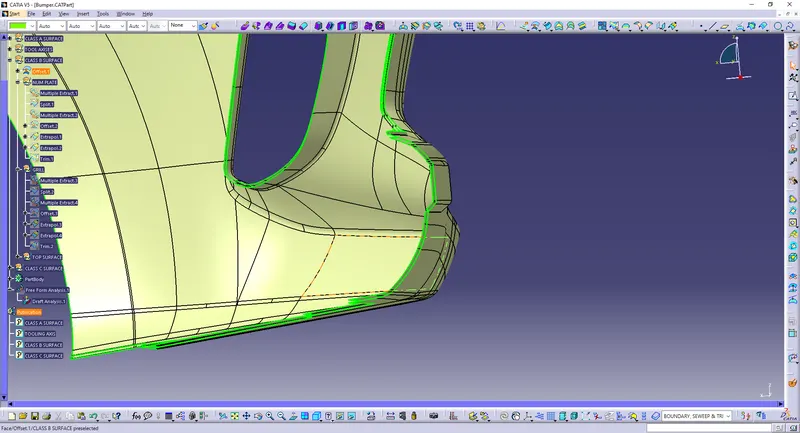
Fig. 8 & 9.
STEP 2:
Then create the bordary in Class B Surface which we want to create new surface of the number plate are shown below. 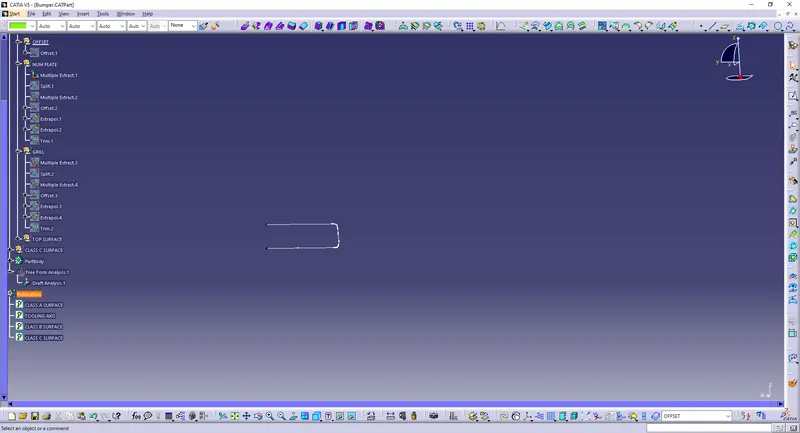
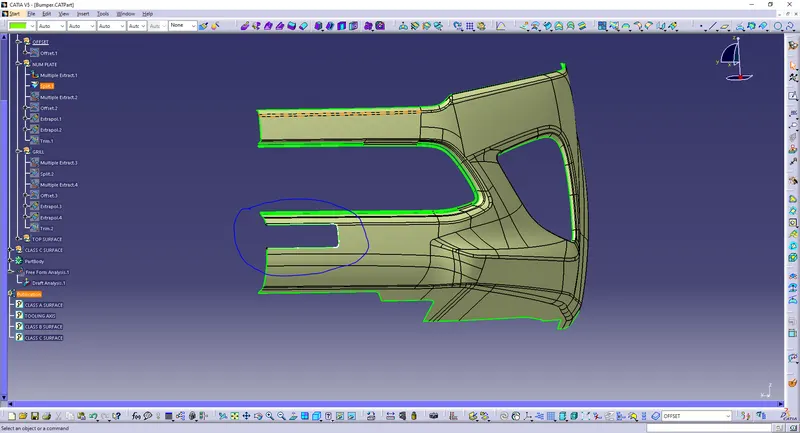
Fig. 10 & 11.
STEP 3:
Extract form the Class A Surface which we need part or surface are shown below.
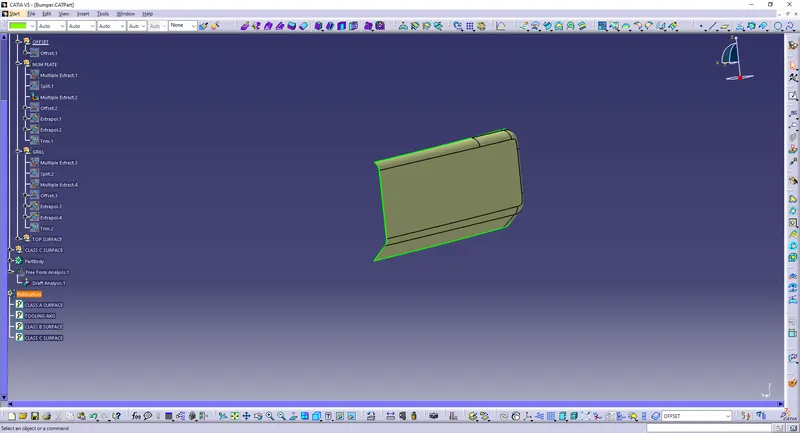
Fig.12.
STEP 4:
Offset every surface with 3mm of it and the image is shown below.
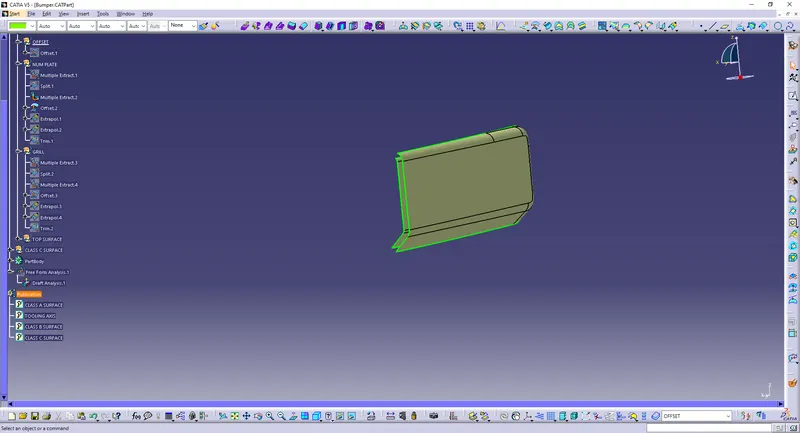
Fig. 13.
STEP 5:
After offset it we have to extrapolate each an every one of it are shown below.
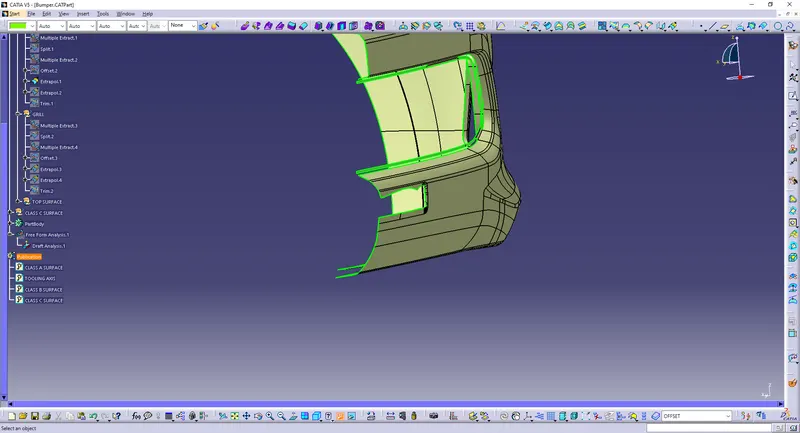
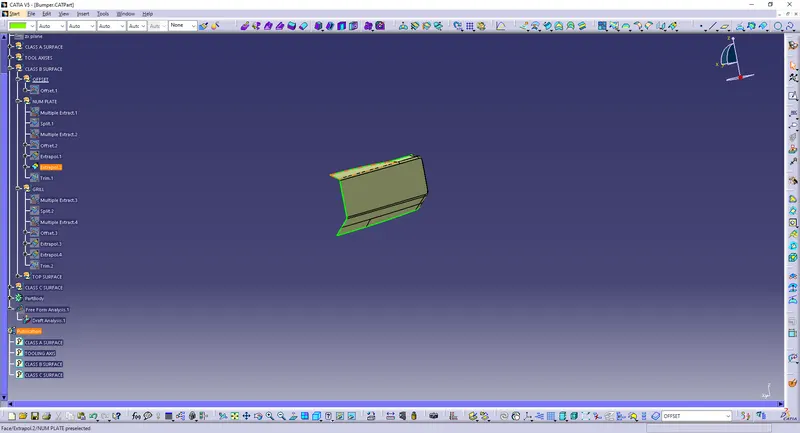
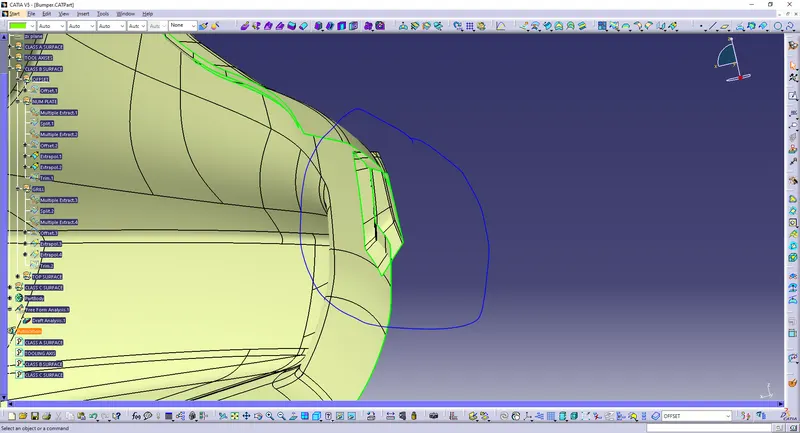
Fig. 14, 15 & 16.
STEP 6:
Trim tool is use to trim all the extra edges of the previous one of it are shown below.
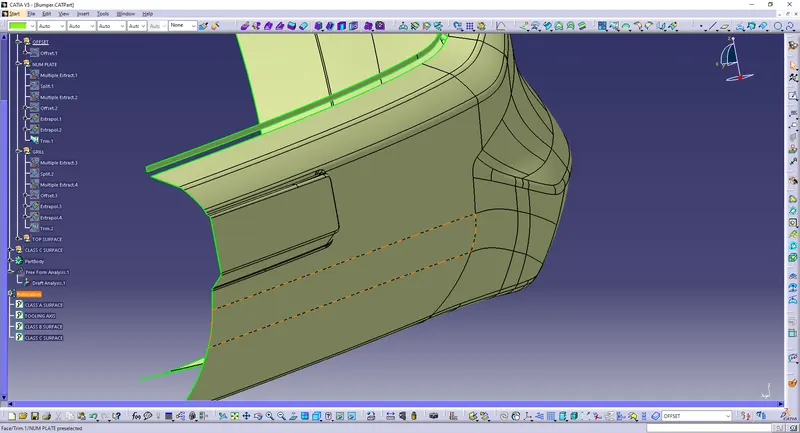
Fig. 17 & 17.1.
STEP 7:
Then create the bordary in Class B Surface which we want to create new surface of the GRILL are shown below.
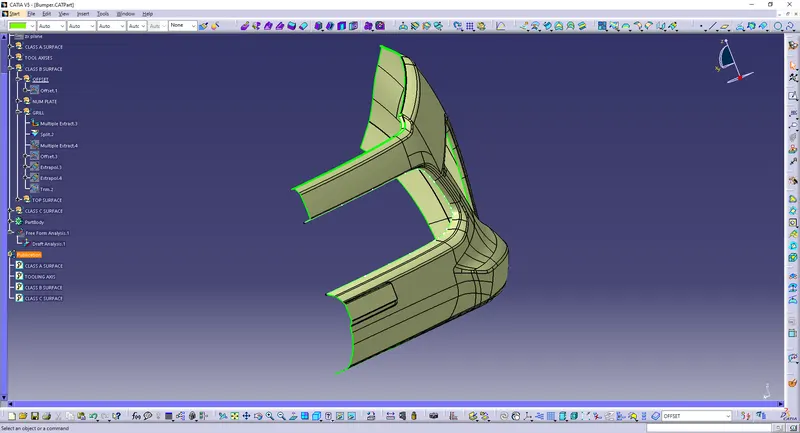
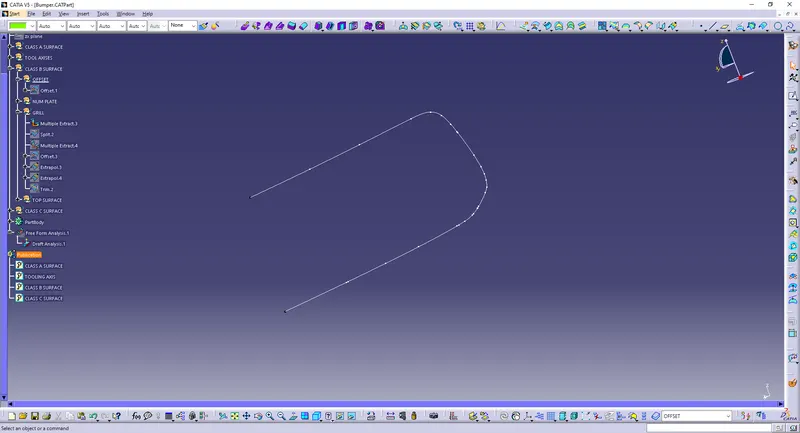
Fig. 18 & 18.1.
STEP 8:
Offset every surface with 3mm of it and the image is shown below.
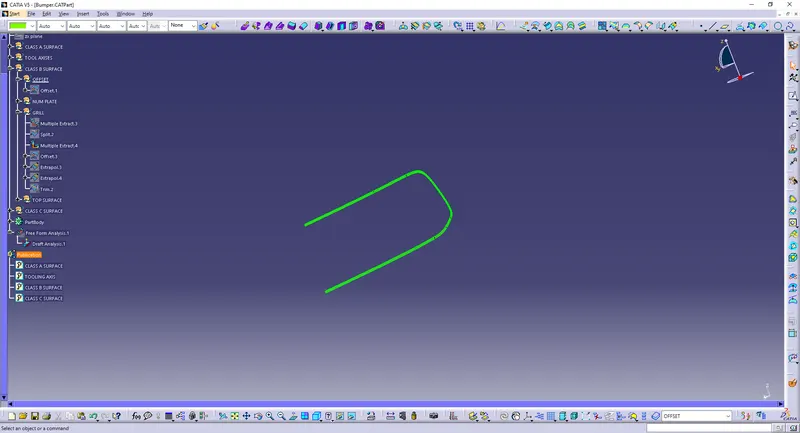
Fig. 19.
STEP 9:
After offset it we have to extrapolate each an every one of it and trim it are shown below.
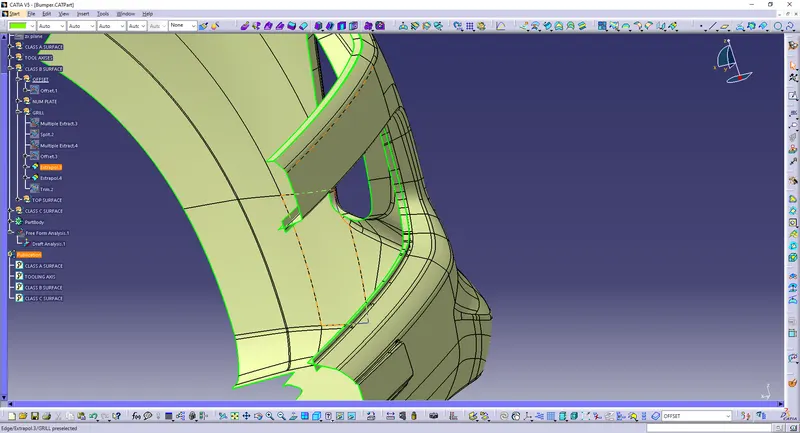
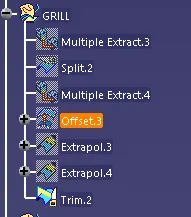
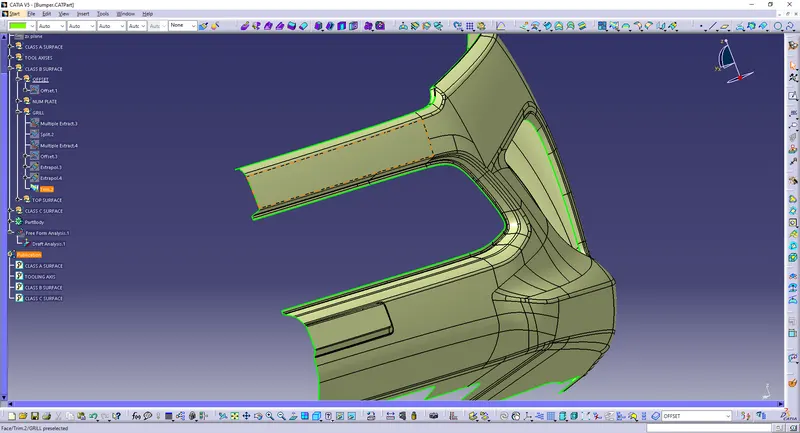
Fig.20, 21 & 22.
STEP 10:
Then create the bordary in Class B Surface which we want to create new surface of the TOP SURFACE are shown below.
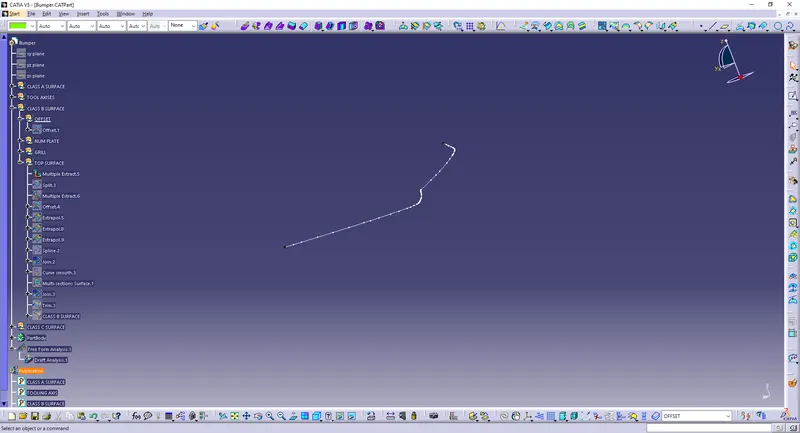
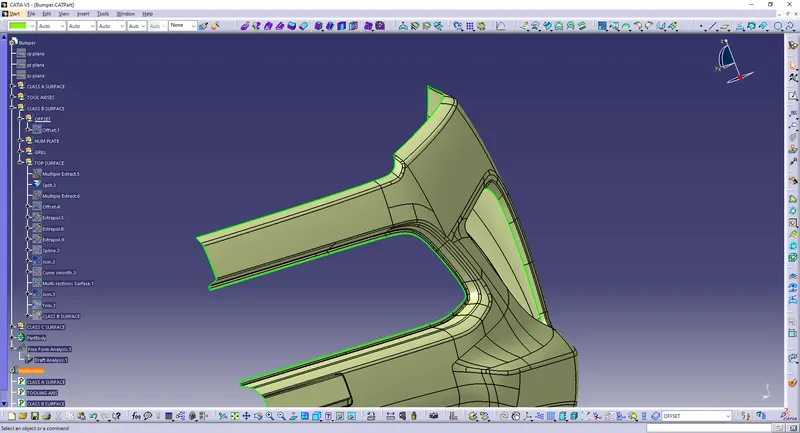
Fig. 23 & 24.
STEP 11:
Offset every surface with 3mm of it and the image is shown below.
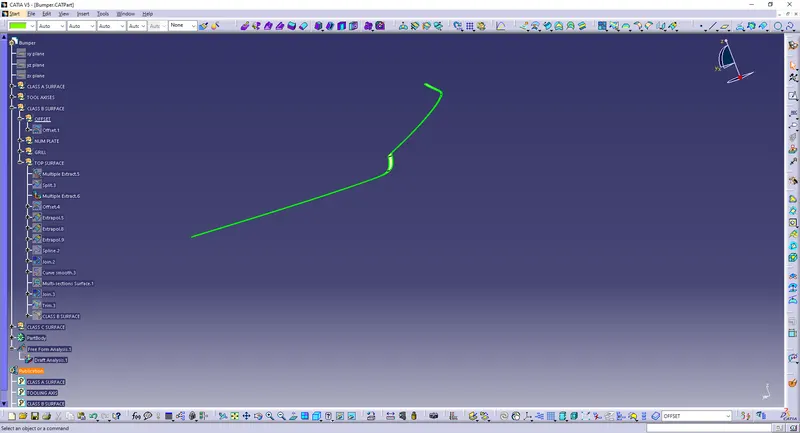
Fig 25.
STEP 12:
After offset it we have to extrapolate each an every one of it and trim it are shown below.
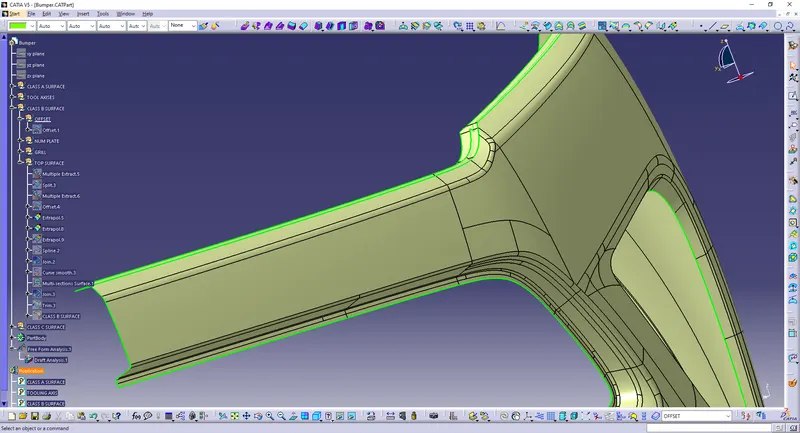
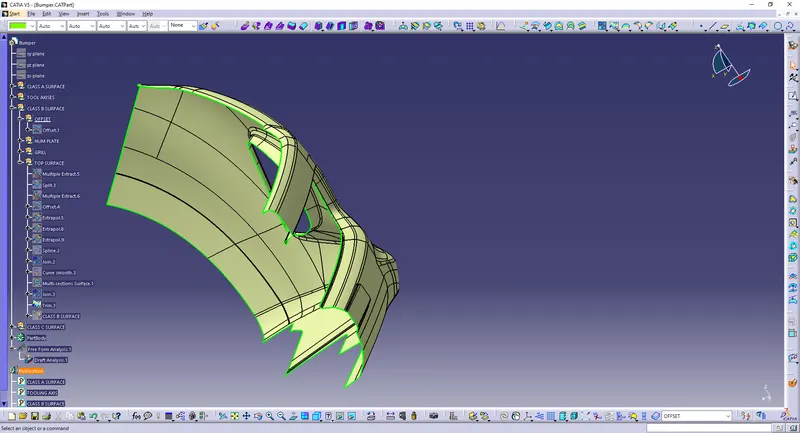
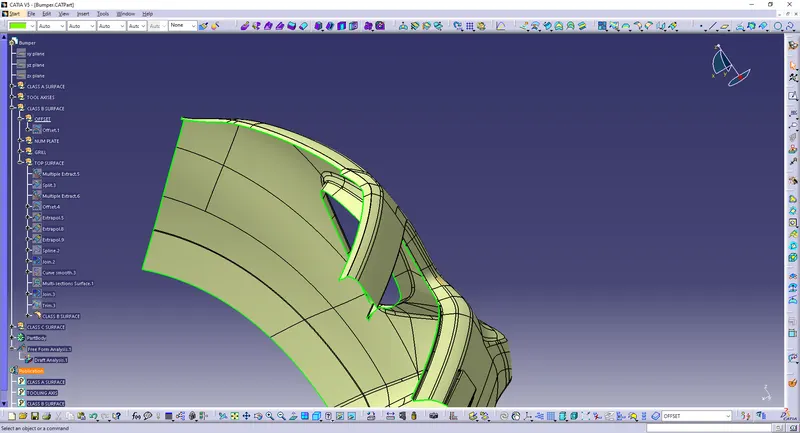
Fig 26, 27, & 28.
Class C Surface:
C surface has been created from the boundary lines of class A surface and by extracting the supporting surfaces then sweep the boundary lines with reference to the extracted surfaces.
In order to get the C surface first we have to create a boundary lines of class A surface or by using multiple extrapolated command and check for the continuity of it.
Create a sweep with reference to the curve and the reference surface with a 90 degree angle and give the inside direction Check for the continuity of the surfaces if there is any gap go for extrapolated and trim all together now we will get the class C surface.
Then join the class A surface and C surfaces together by join command then check it for connectivity of the surfaces if it is ok then finally trimmed it with B surface we will get the final component again check whether the final body is closed by using boundary command.
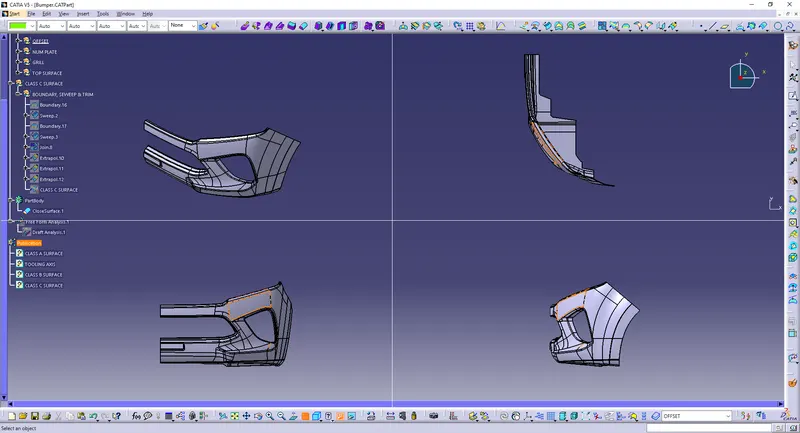
Closed solid body is created by using the close surface on part workbench by selecting the final Trimmed component and do the draft analysis for the same.
Class C Surface as shown as img. are given below:
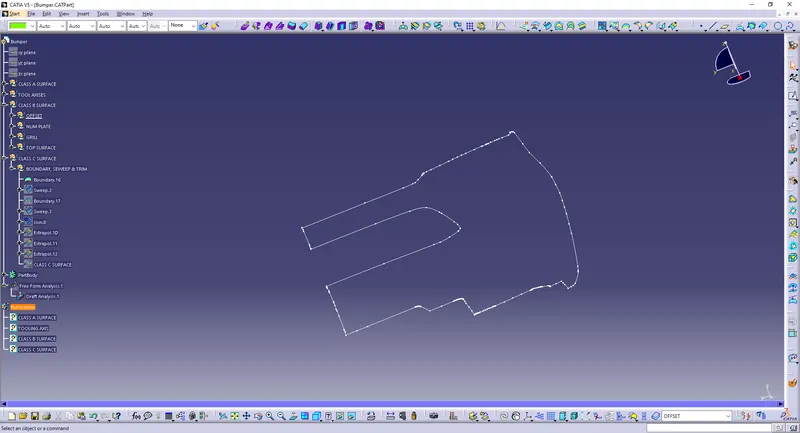
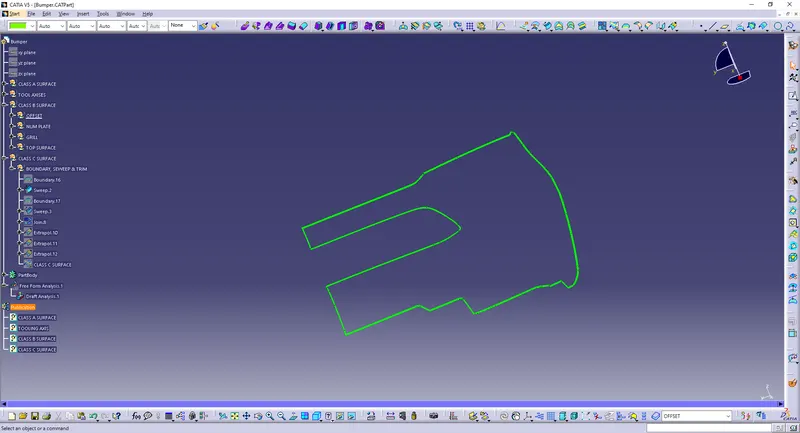
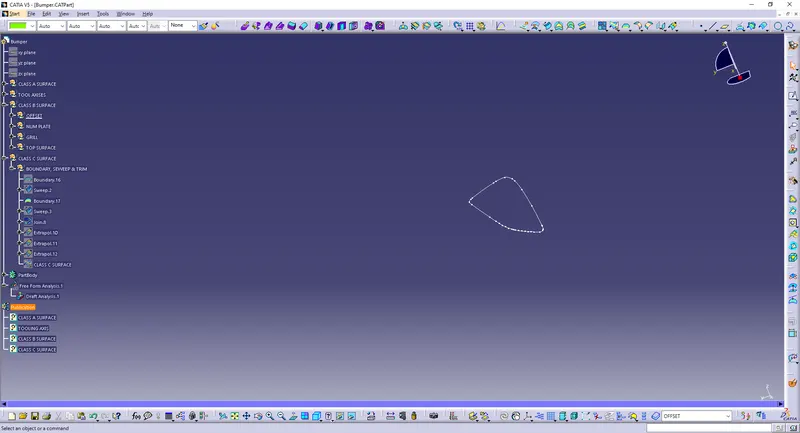
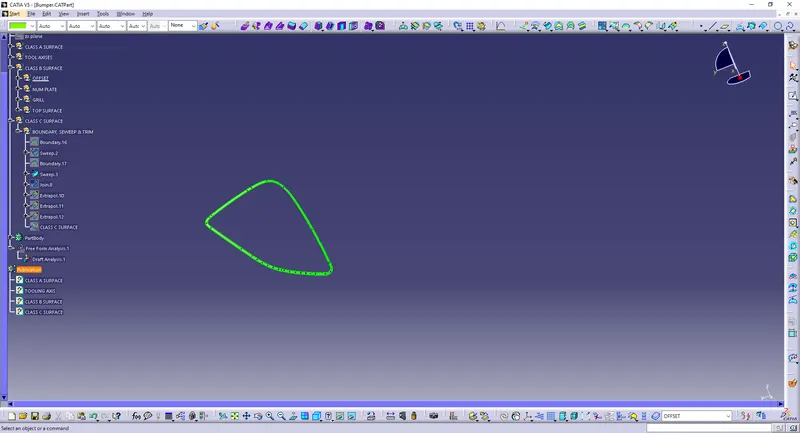
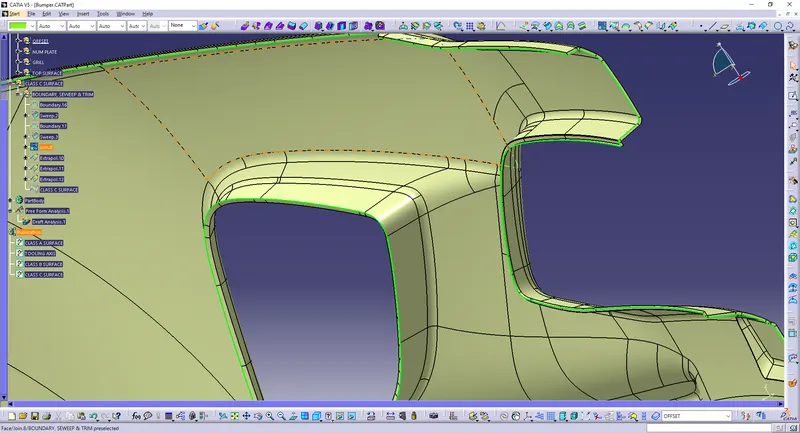
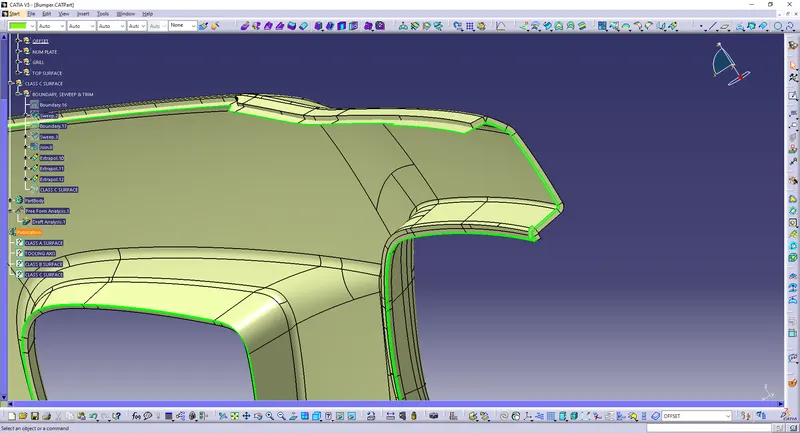
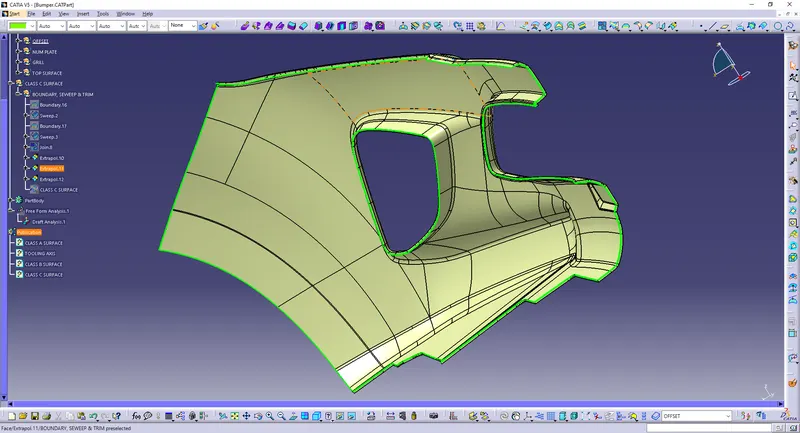
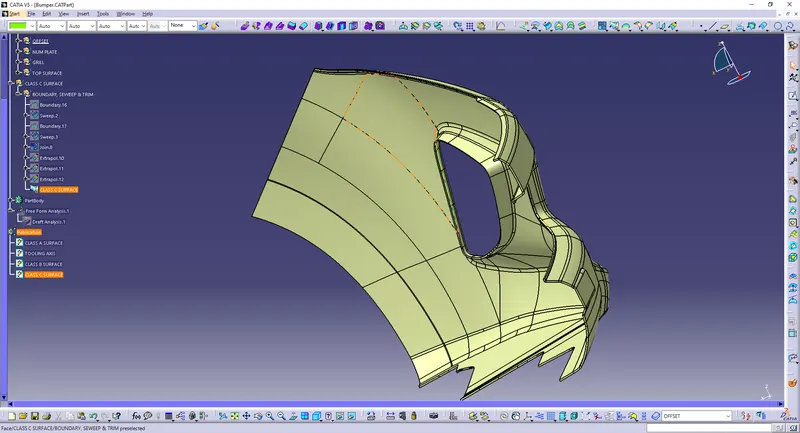
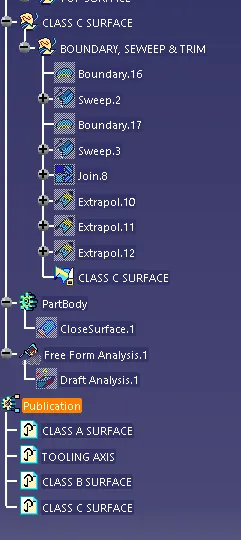
Fig. 29.
CONCLUSION:
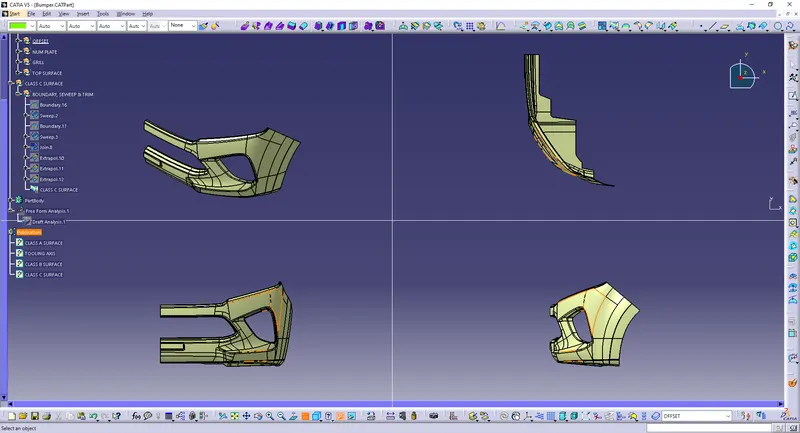
The drafting also take place over here wether the part is maufactureable are not are shown below.
The part is coverted to soild also are shown below.
Finally the Class – A, B & C surfaces with the Tooling Direction have been Published and the Bumper is moved on to the designing of the next operation – the creation of B-side features.
Final product img. are given below:
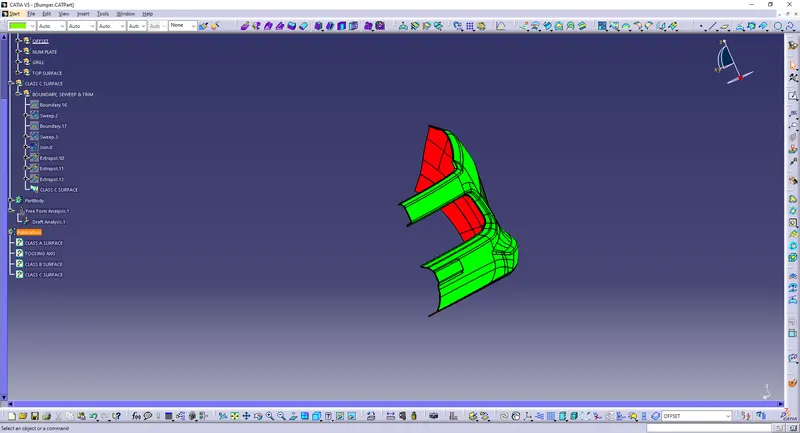
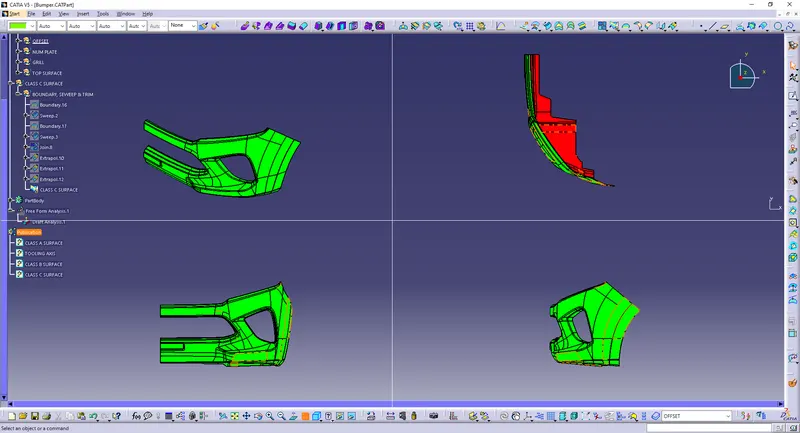
THERMOSET PLASTIC:
I refer Acrylonitrile Butadiene Styrene, or ABS plastic.
Acrylonitrile Butadiene Styrene, or ABS plastic, is an opaque thermoplastic. It is an amorphous polymer comprised of three monomers, acrylonitrile, butadiene and styrene. ABS is most commonly polymerised through the emulsification process or the expert art of combining multiple products that don’t typically combine into a single product.
When the three monomers are combined, the acrylonitrile develops a polar attraction with the other two components, resulting in a tough and highly durable finished product. The different amounts so f each monomer can be added to the process to further vary the finished product.
The versatility of ABS plastic properties contributes largely to its popularity across several industry sectors. From computer keyboard keys to LEGO, products made from ABS can be found all around the world in multiple domestic, commercial and specialist settings.
ABS material Properties
The acrylonitrile in ABS plastic provides chemical and thermal stability, while the butadiene adds toughness and strength. The styrene gives the finished polymer a nice, glossy finish. ABS has a low melting point, which enables its easy use in the injection moulding process and 3D printing. It also has high tensile strength and is very resistant to physical impacts and chemical corrosion, which allow the finished plastic to withstand heavy use and adverse environmental conditions.
ABS can be easily moulded, sanded and shaped, while its glossy surface finish is highly compatible with a wider range of paints and glues. ABS plastics takes colour easily, allowing finished products to be dyed in exact shades to meet precise project specifications.