Design of backdoor
Aim:
To design the Back door (Tail gate) of a car from the styling surface provided using NX CAD. The ultimate aim is to design the Back Door by following the Industrial Standards.
Back Door:
A back door is a BIW(Body In White) component found in all Automotive car generally used for opening and closing of the so called car luggage that is usually used for storing items inside a car. In general the opening and closing of the door is coordinated by the Latch and Striker position and the Gas stay position that is mounted on the body and back door of the car. These positions play a major role in ensuring smooth opening and closing of the tail gate.
Parts of a Tail Gate:
- Outer Panel
- Outer panel Lower
- Inner panel
- Hinge Reinforcements
- Latch and Striker Reinforcement
- Wiper Motor Reinforcement
- Gas Stay Reinforcements
All these parts are assembled together to obtain the back door of a car.
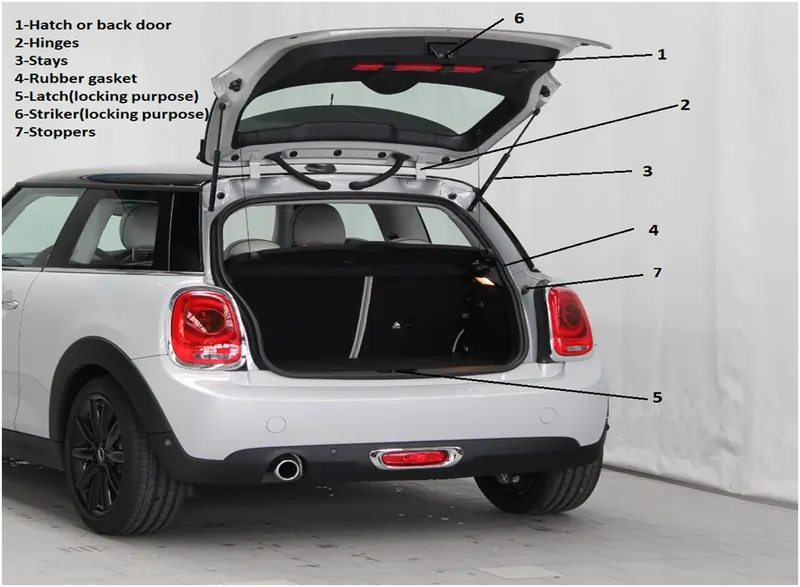
Fig - Components Of Backdoor
Types of Back Doors:
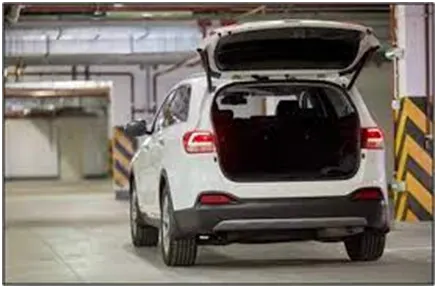
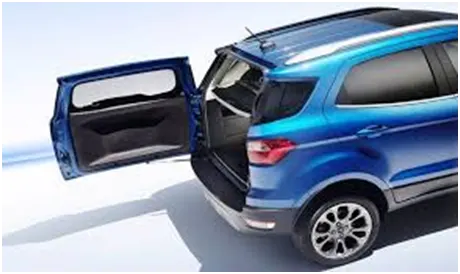
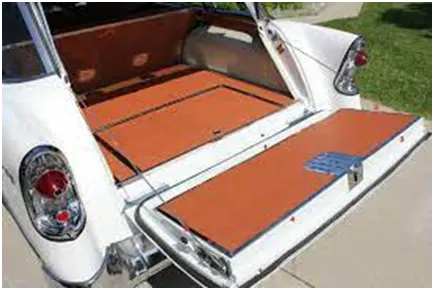
There are three types of back door based on the position of the Hinge axis. They are
- Top Mounted
2. Side Mounted
3. Bottom Mounted
In our design we follow the Top Mounted Design where the Hinges are mounted on the top.
Design Considerations In Back Door Design:
The following are the Design considerations taken while designing the Back Door. They are,
- Visibility Criteria
- Force Dissipation
- Latch and Striker Positions
- Hinge Position
- Gas Stay Position
- Material Selection
- Space Availability
- Hemming and Relief Areas
All these design considerations go hand in hand with each other because these positions are dependant on each other and if position gets altered all the positions has to be altered for effective opening and closing of the back door. The Latch and Striker, Hinge Position and the Gas stay Positions has to be maintained in a proper way so that they play a major role in the opening and closing as well as the rear Visibility criteria of the car.
Processes used in manufacturing of a Backdoor:
- Blanking and Piercing: Blanking and piercing are shearing processes in which a punch and die are used to produce parts from sheet stock. Blanking produces the outside features of the component, while piercing produces internal holes or shapes. The web is created after multiple components have been produced and is considered scrap material. The “slugs” produced by piercing internal features are also considered scrap.
-
Deep Drawing: Deep drawing is one of the most widely used processes in sheet metal forming. The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions. A flat sheet metal blank is formed into a hollow body open on one side or a hollow body is formed into a hollow body with a smaller cross-section. This process is considered “deep” drawing when the depth of the drawn part exceeds its diameter.
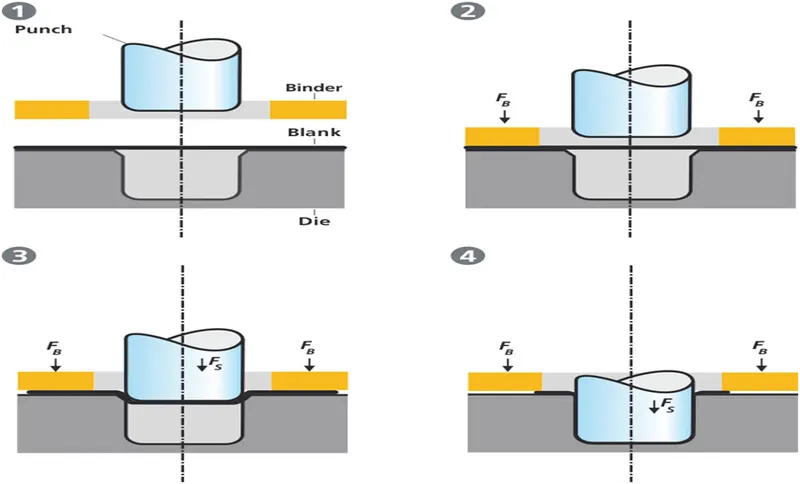
Fig - Deep Drawing
- Embossing: In sheet metal embossing, the deformation of the metal takes place because of stretching of the metal (or tensile force acting on the metal), due to which the sheet metal is subjected to excessive thinning and fracturing. Sheet metal embossing is generally used to create logos, lettering, small depressions, etc.
Thus the depth to which the material is depressed depends upon the thickness of the sheet as well as stretch ability of the material.
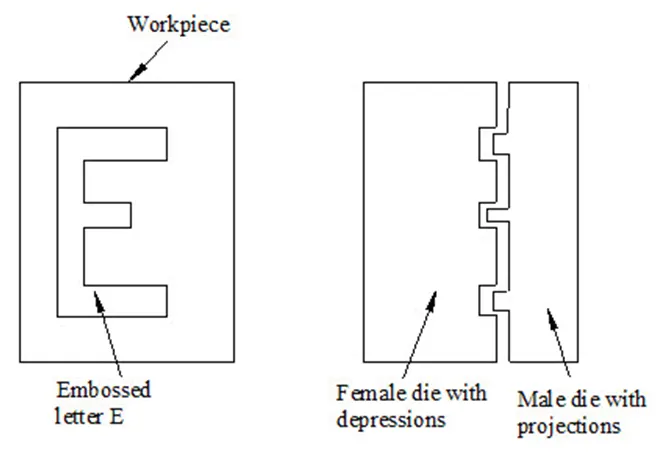
Figure – Embossed Design
- Hemming: Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. Or we can say that Hemming is a sheet metal forming process in which sheets are joined by bending it usually to 180°. Automotive body panels and automotive parts such as deck-lids, trunk-lids, doors, hoods and tailgates are formed by hemming process.
Mastic Points: These are the spots where the inner panel and the outer panel of hood are joined or can say that they are sealed together using a mastic glue. If processes like welding, bolting, etc are used at the place of mastic points, the hood will lose all its aesthetics. So, mastic sealant is used which is elastic compound and acts like rubber. It is placed between both the panels. Initially it is in paste form and after hot furnace bath it gets solidify and gives strength to the panels together. Generally, One spot of mastic point has influence over diameter of 80 mm.
Material Selection:
The material selection play a major role in determining the overall weight of the back door. The materials generally used are Steel and Aluminium. The Density of Steel is higher than Aluminium thus it results in adding more weight to the door. Basically the material is used based on the budget of the car, because the cost of steel is very cheap than Aluminium. If aluminium is used instead of steel there is no need of many parts like Reinforcements for each mounting and the overall weight get a reduced by 6-10 kg approximately. But the drawback is Aluminium is much costlier than Steel. Hence based on the budget of the car aluminium is used. In higher end models like Benz, Audi, Porshe and BMW we can find aluminium is used instead of steel resulting in reduced weight and increased performance of the vehicle.
Another Factor to make a note is using Casted Aluminium instead of deep drawn Steel components and adding reinforcements to it. Hence, the space of the luggage commodity gets increased by a certain amount because the draft angle for Casted aluminium is much lesser (3 degree) than the deep drawn Steel inner panel (7-9 degree). Thus it reduces the space between the inner and outer panel resulting in much larger cabin space than the deep drawn steel inner panel. Thus the material selection is one of the design consideration taken. Since it reduces the space between the inner and the outer panel, the rear visibility of the car is also improved giving more space for the mirror to view.
Hence in this design, the material chosen is steel since it is designed for a medium budget car and hence high cost could not be afforded to design the back door.
Force Dissipation:
The major criteria in designing the backdoor or any BIW part is the force dissipation during an impact or a collision. Hence studies are being done in order to dissipate the force on the sides and avoiding it to reach the inner cabin of the car so that possible damage of impact inside the car is reduced. Hence in order to do that the V or Y embosses are created on the inner panel so that the force gets transmitted on to the sides instead reaching it on the cabin. This is one of the main criterias in back door design.
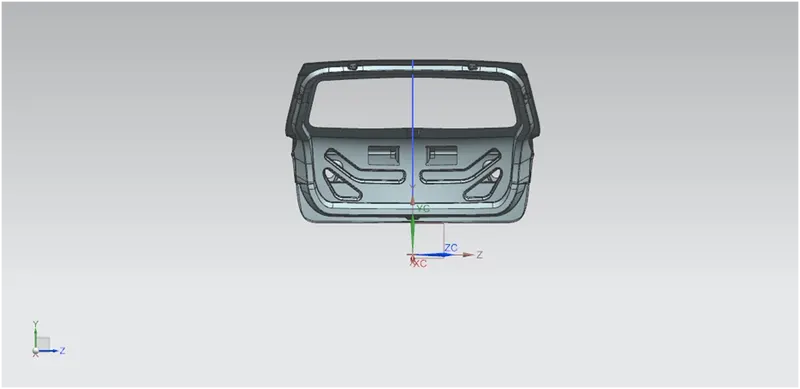
Figure - Force Dissipation
Thus from the above image it is clear that the forces are dissipated on the sides instead of reaching inside. This is the reason to have Y or V embosses on the panel to increase the stiffness and to dissipate forces onto the sides.
Latch and Striker Positions:
The Latch and Striker positions play a major role in determining the opening and closing of the back door. Hence the opening and closing of the had to smooth and in order to ensure that the centre point of the latch and striker has to be at the same point and the trajectory has to be tangent to the open close circle that is drawn. This is shown in the below image. Only if the centre points and the tangent line are perfect the opening and closing of the back door is smooth and clear. Or else the Hinge positions, Gas stay positions and Latch and Striker Positions has to be altered to meet the change.
Hemming and Relief Areas:
Hemming and Seaming are two similar metal working processes in which sheet-metal edge is rolled onto itself. Hemming is the process in which the edge is rolled flush to itself, while a seam joins the edge of two materials.
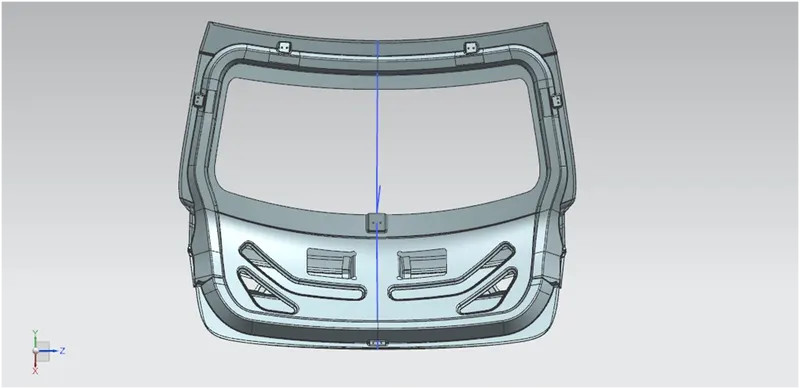
Figure - Hemming and Relief Areas
The Hemming is done on the outer and the inner panel with a clearance of 0.2mm on the either sides. Since at the corners the hemming is difficult to perform, clerances has been given at the ends of panels so that it would for the hemming operation is performed. Here is the image of the hemming relief at the corners.
Parts of the Back Door Assembly:
1) Outer Panel
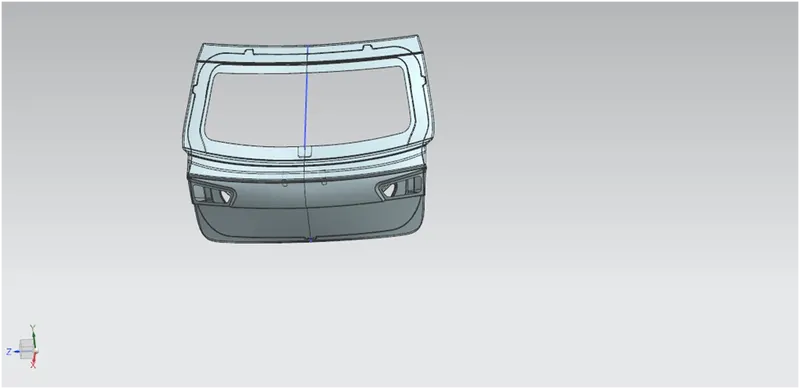
Figure - Outer Panel of Backdoor
2) Inner Panel
Figure - Inner Panel of Backdoor
3) Reinforcements:
Reinforcements are generally used to increase the strength of the mountings so that there is no un-necessary dents or noise occurs at the time of motion. This does not only add strength to the part but also increase the overall stiffness of the part so that the part is completely stable. The Reinforcements used are
1) Latch and Striker Reinforcement
2) Wiper Motor Reinforcement
3) Hinge Reinforcement
4) Gas Stay Reinforcements
The Following Image shows the reinforcement that are used on different areas of the inner panel. They are usually spot welded on the inner panel.
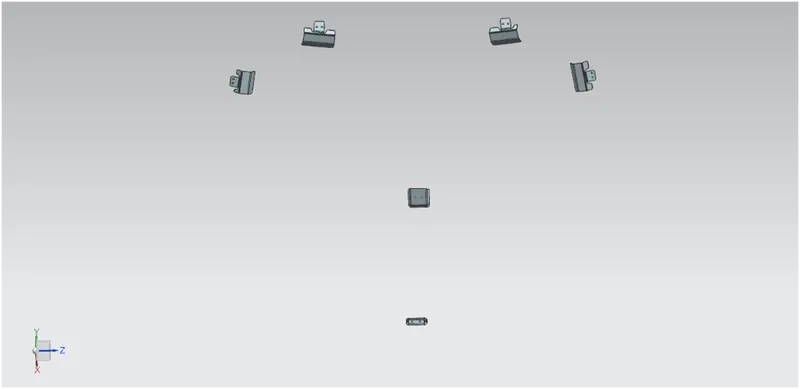
Figure – Reinforcements in Backdoor
Conclusion:
Thus the designing of the Back Door or Tail Gate is done as per Industrial standards and Manufacturing Techniques.