Design of backdoor
AIM:
To design the back door of the car and make the inner panel for the back door and also design the necessary
re-inforcements.
INTRODUCTION:
The trunk or boot of a car is the vehicle main storage or cargo compartment often a hatch at the rear of the vehicle. it is also called a tailgate. These doors can be operated manually or electricpowered.In the most of the luxury cars door s electrically operated. involves a very major role during rear crash cases. so our design must be obey crash requirments the institude of highway saftey analyse the different accidents and they set a test to rate our car. so these rataing depends upon the design of the trunk and material used, flenges, embosses, type of joining of inner panel and outer panel etc.
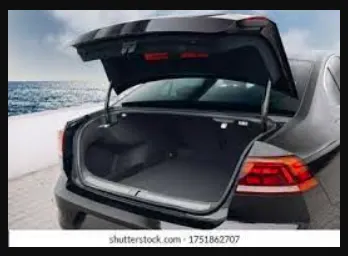
Types of doors based on working position,
1. Top Mounted Door
2.Side Mounted Door
3.Bottom Door
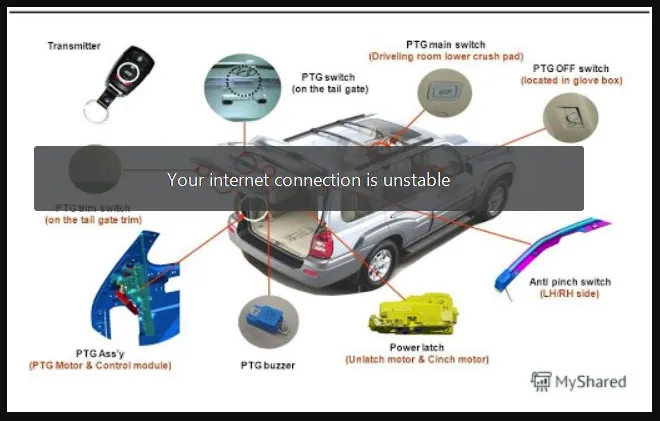
the back door is operated by two types of comodities
1.Electrically operated
2.Gas stay powered
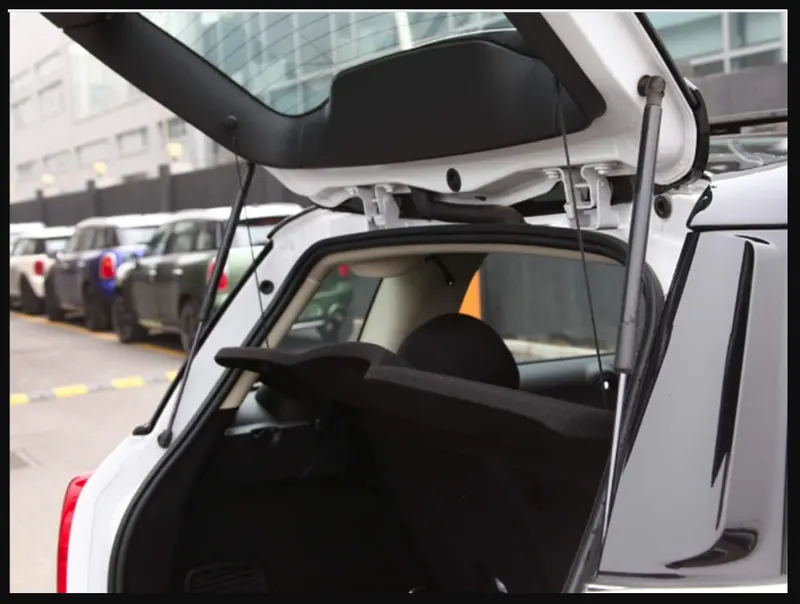
1.Gas stay powered
The main purpose of these mechanisims is to open the back door without heavy efforts,becausethe backdoor have different parts and the weight of the back door is high, so we are not able to open the back door manually, so we introduced these two types comodites. and these also decided the prmium of the car, mostly the electrically operated used in premium cars.
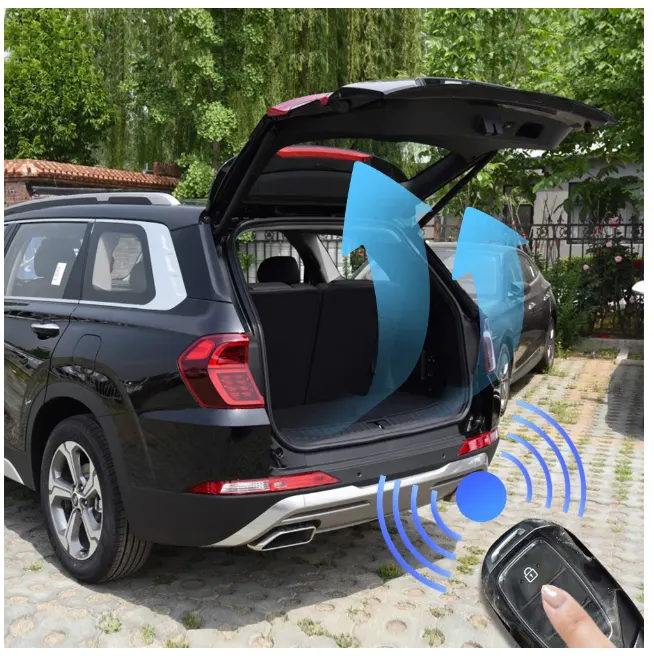
2.Electrically operated
Electric tailgate for HYUNDAI santafe car intelligent remote control power operated tail gate opening closing rear door lifting Trunk Lids & Parts
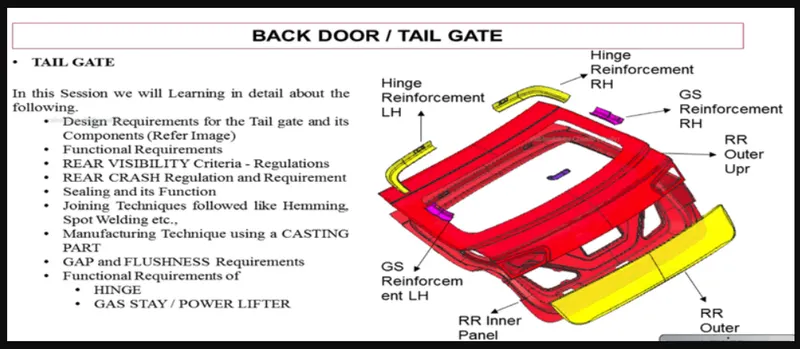
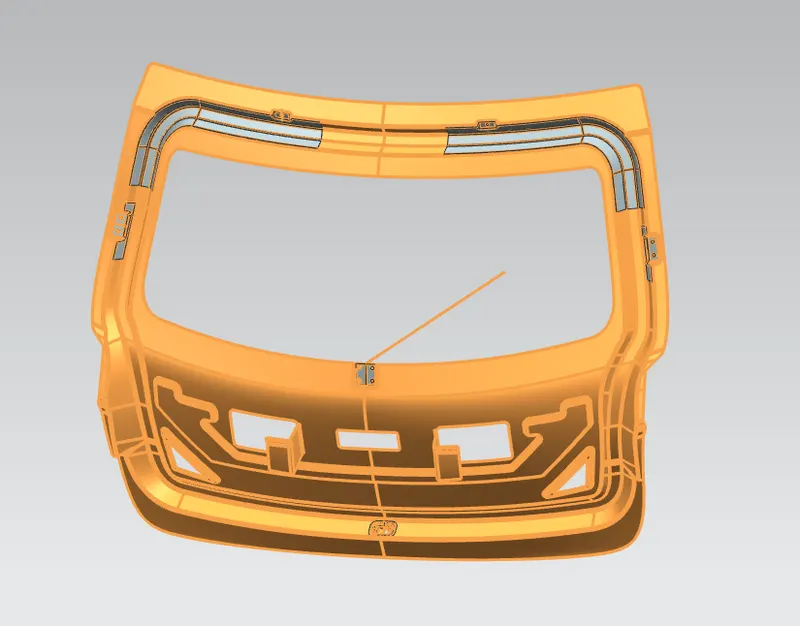
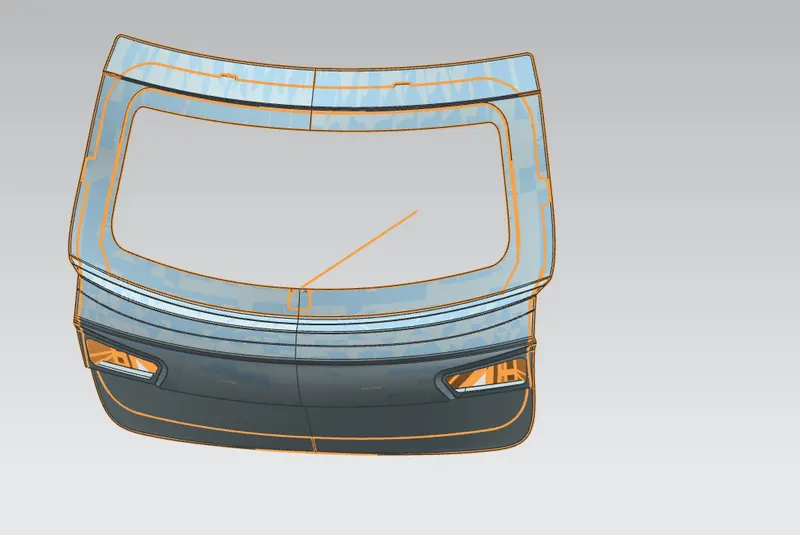
Back Door Assembly:
1. Inner panel
2. Outer panel
3. Hinge and its reinforcement
4. Wiper motor reinforcement
5. latch & stricker and its reinforcement
6. Gas stay reinforcement
******
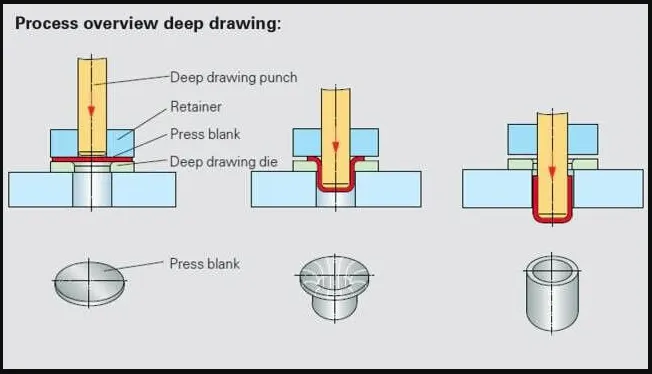
the majorproblem in back door is material selection, mostly in past days steel is used, but it makes a very problems the steel parts have heavy weight, so it reduces the fuel economy, insted of steel presently in high end cars aluminium is used ,the main objective of aluminium it have less desnser material and its sutaible for complex shapes, and it also gives the thickness locally because it done cating, in case of steel we used deep drawing operation.there are some of the advantages and disadvantages are there.
******
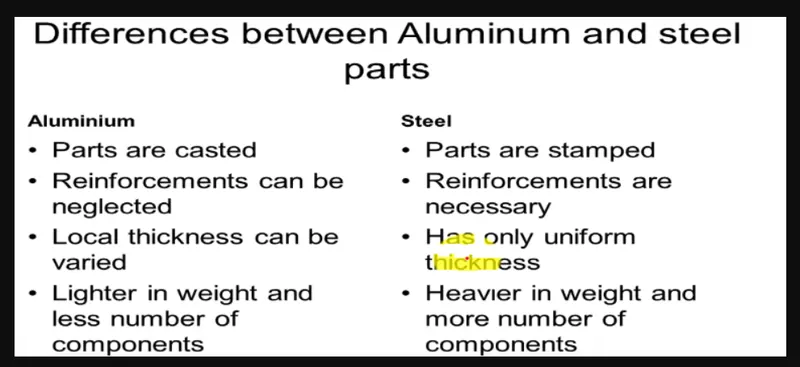
so by using of aluminium we can reduce the number of parts and assembly involvement and it is castly material.
******
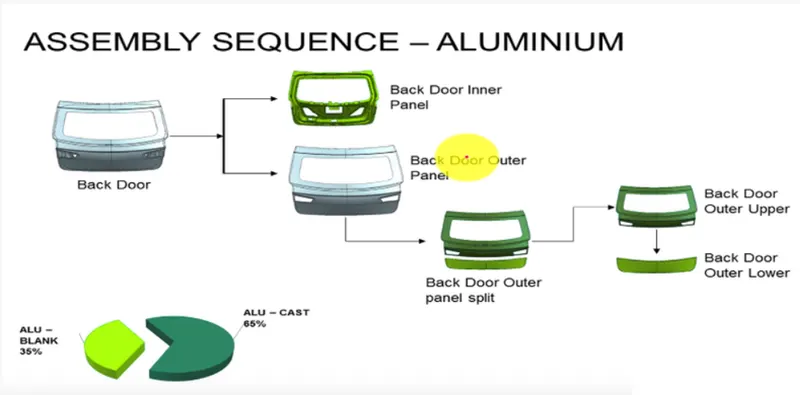
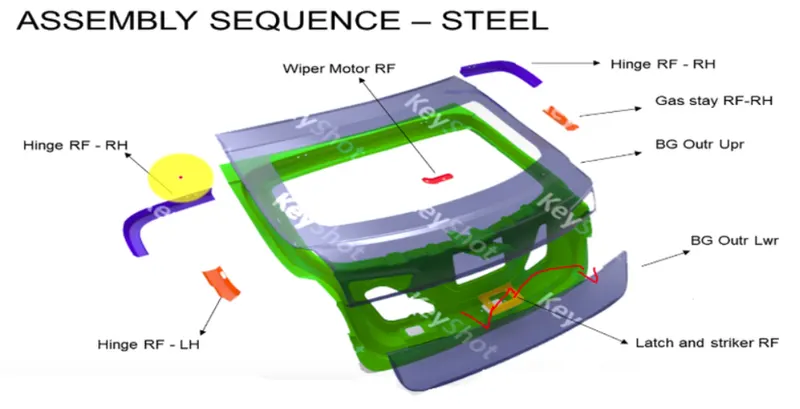
Different types of sheetmetal operations are done in the Back door deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
1. First - Stage drawing : The blank shape of metal s placed onthe die and contact with the punch. Initially the panch moves in downward direction. The outer ring of blank is subjected to pure radial drawing. Between die and blank metal. The metal become a bent and sliding over die also stretched between die and punch. The metal in pisnity of punch head and contact with it bend and slide over radial and stretch over punch head.
2. Redrawing : The components drawn from first stage again it is redron convert into more death to form a cup shape in the die and punch. The second stage of drawing is called as red drawing.
Embossing embossing is a metal forming process for producing rice or sun can design or relief in sheet material by means of match male and female roller dies. Theoretically with no change in metal fitness or by passing sheet or a strip of metal between roles of their desired pattern. Metal sheet is throw the male and female roller dice producing a pattern or design on the metal sheet. Depending on the roller dice used different patterns can be produced on the metal sheet.
Materials commonly used in the metal imposing process include.
1. Aluminium malai
2. Steel alloys.
3. Zinc
4. Copper
5. Galvanized steel
6. Brass
7. Cold rolled steel
hemming:
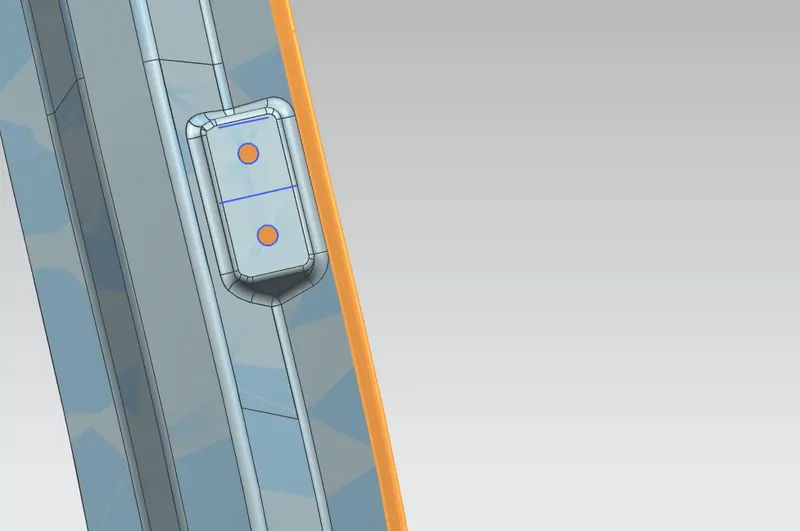
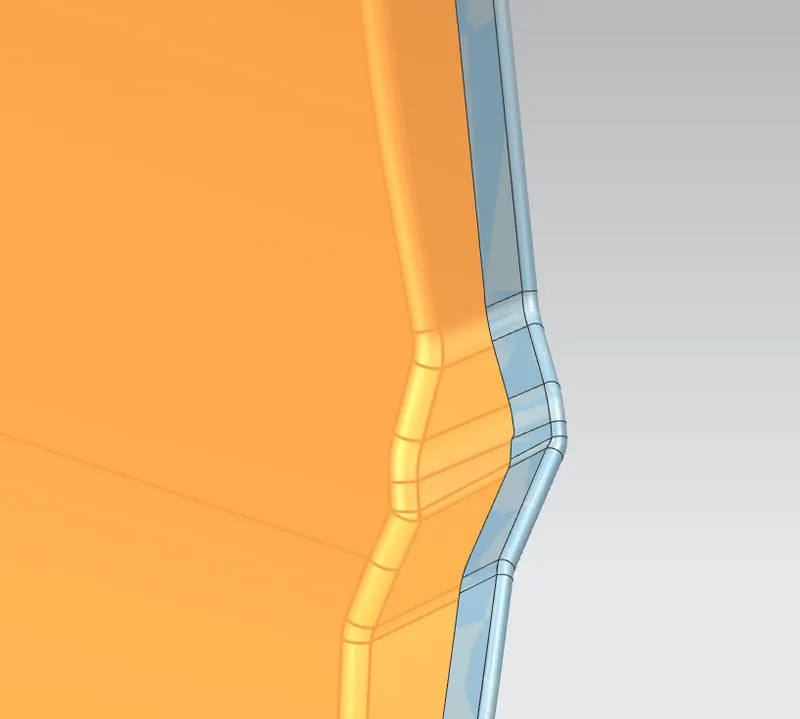
Heming is a forming operation in which the edges of sheet are folded or folded over another part in the order to achieve a tight fit. Normally hanging operations are used to connect parts together to improve the appearance of a pot and reinforce edges
In carp production haming is used in assembly as a secondary operation after deep drawing dreaming and flanging operations to join two sheet metal parts outer and inner together. Typical parts for this type of assembly or who's doors trunk lips and defenders. They are various types of heming operations.
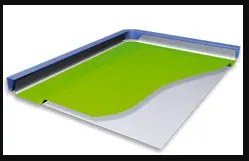
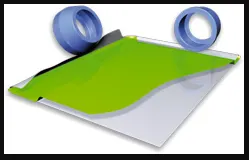
1. Conventional die hemming:
In conventional Di hamming the flange is folded over the entire length with a hemming tool.
2. Roll hemming:
Hindi role humming the heming roller is guided by an industrial robot to form the flange.
Open Hem: A hem haisha full round future and a return flange. In open heming bend angle is equal to 180 degrees.
Tear drop hemming: inter drop and the be banned angle is greater than 180 degree.
Closed hemming: hems without any inside radius are called as closed heming closed hemings or not recommended if the hemming geometry is to be painted or if the material used in SST or aluminium.
Blanking: Blanking Asia cutting operation of flat metal sheet and the article punched out is now as blank. Required product of the operation and the metal left behind is considered as a waste.
Punching: It is similar to blanking only the main difference is that, the whole is there required product and the material punctured out from the whole is considered as a waste.
Inputs for designing of back door:
1. outer panel - 0.75 mm
2. Inner panel - 0.75mm
3. Reinforcements - 1.5mm
Class a surface:
Back door outer upper and lower class surface has to be repaired according to the smoothness. After repairing the surface the door is divided into pots as door outer upper and a door lower panel.
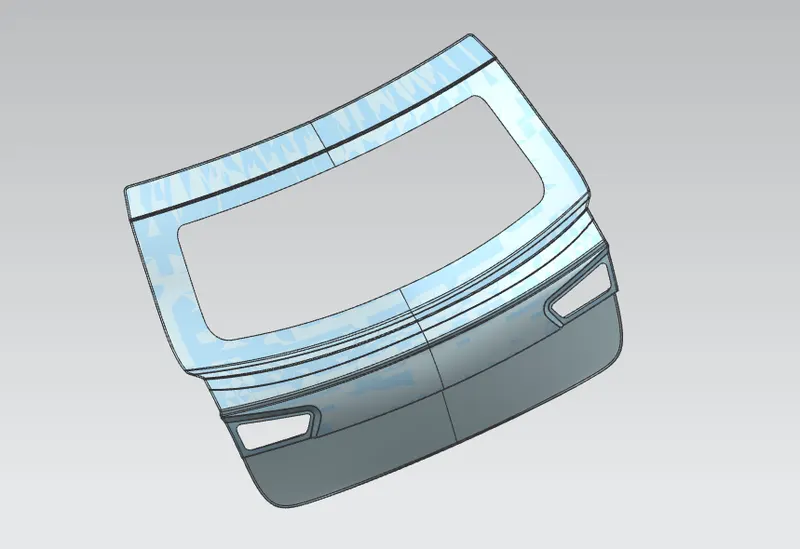
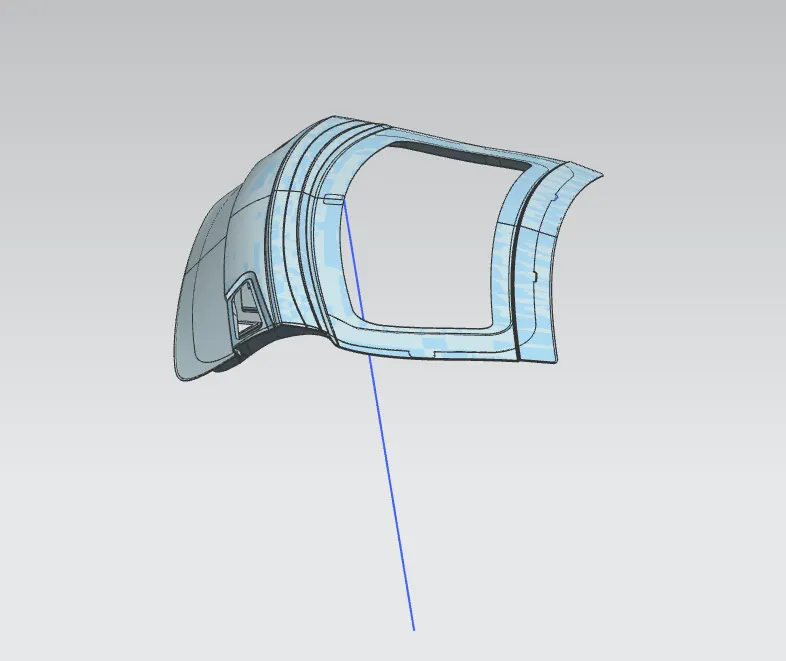
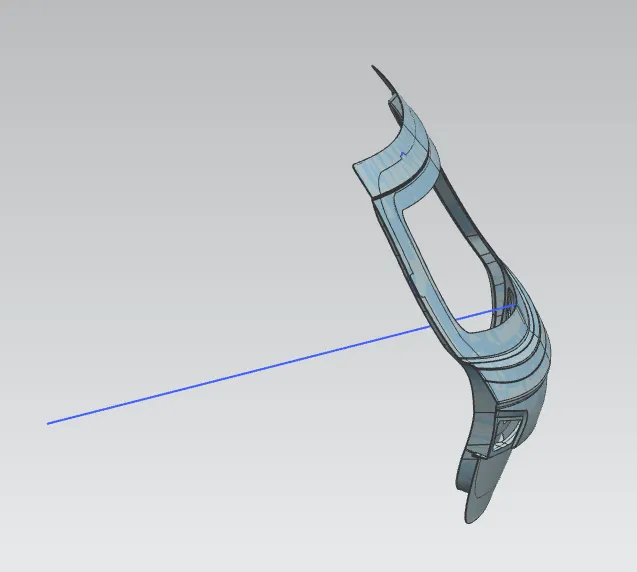
First, we need to create the tooling direction for the deep drawing operation. It shows that all the operations like embossing is done by considering this vector direction and it will help in manufacturing the part,
 ******
After that we have to create sealing Flange by offsetting the outer panel to the specific distance.
Then we will be creating the back door inner panel flange by off setting the outer surface at a distance considering the sheet thickness and thickening direction.
Then created the connecting flange to join the inner panel and sealing flange.
Then for the windshield panel mounting, wing shield panel is created and joined with sealing flange.
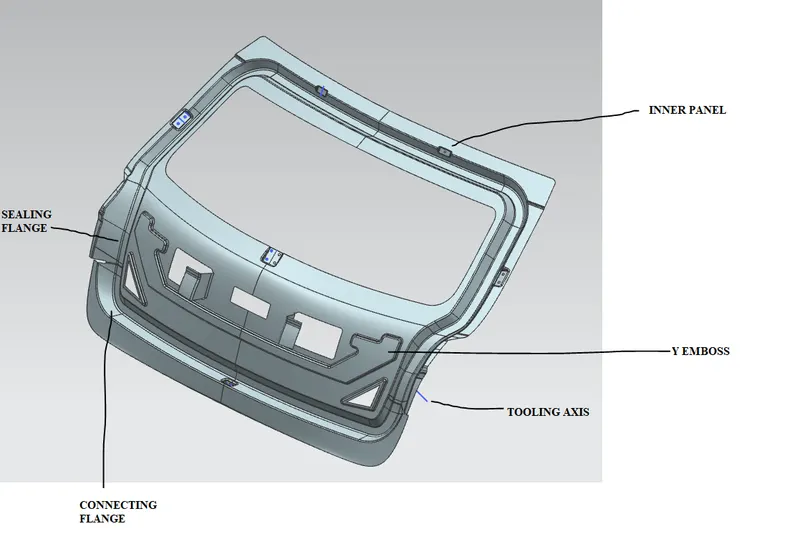
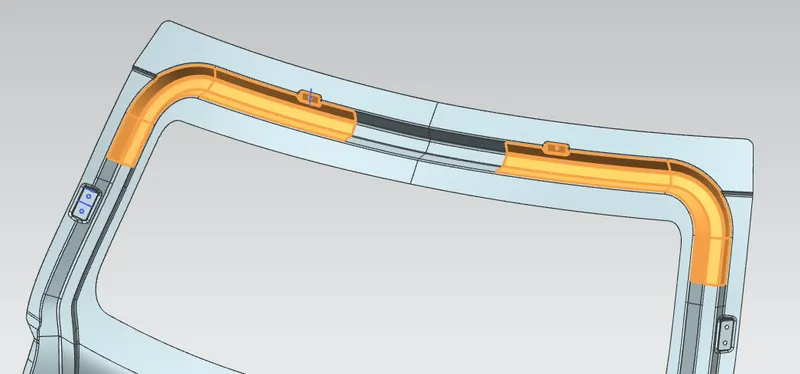
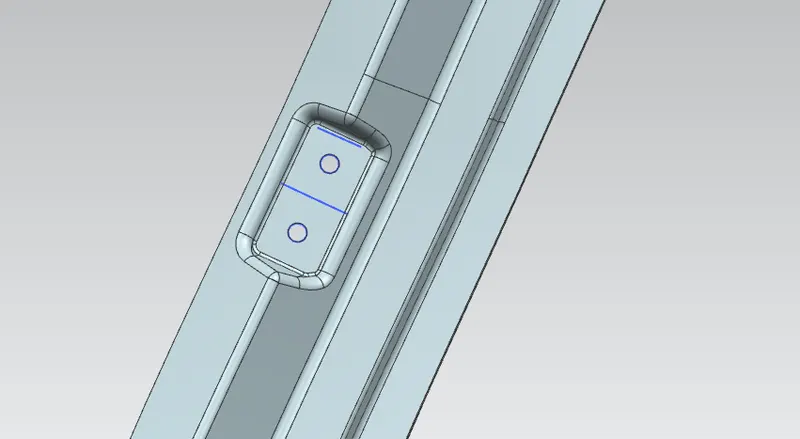
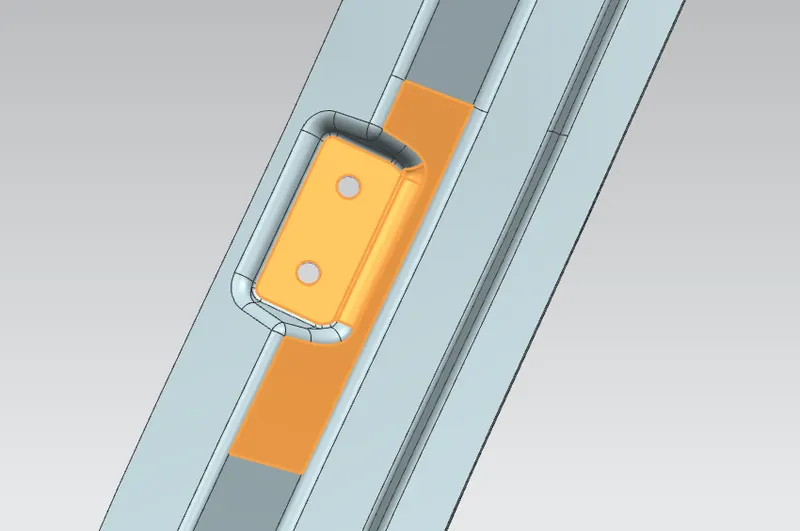
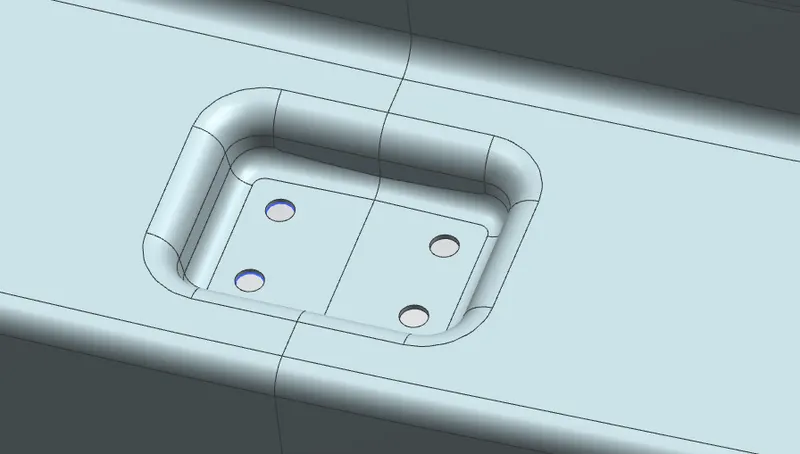
Now to assemble the back door with the veicle hinges are used to open and close teh door. For that to increase the local area strength we have to design the emboss and provide the approprite reinforcement to withstand the load acting upon it.
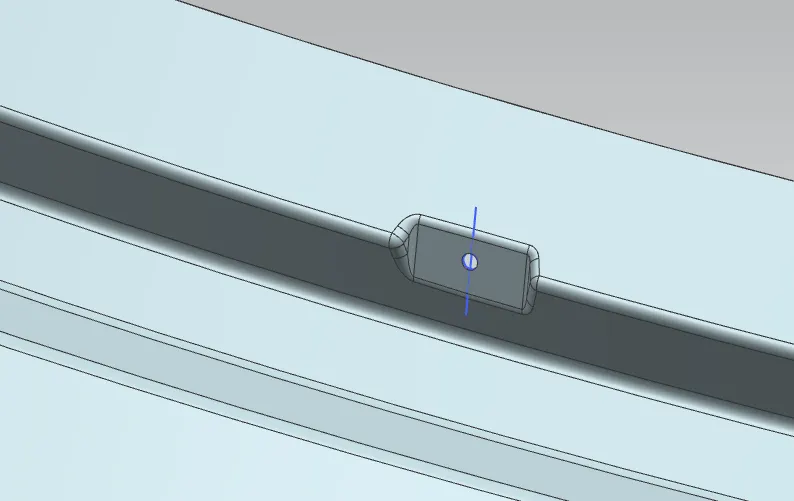 *******
Hinge reinforcement:
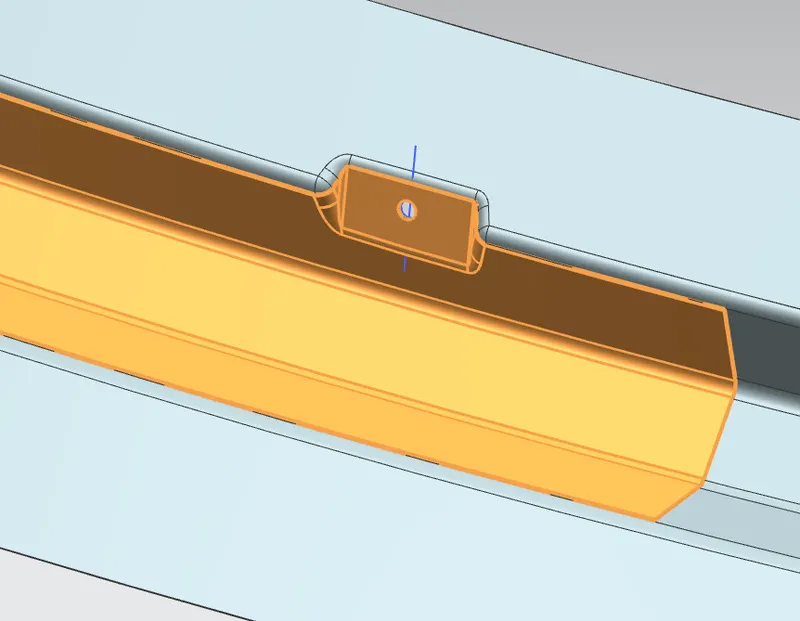
Gas stay Emboss and Reinforcement:
Latch & Stricker Emboss:
 *******
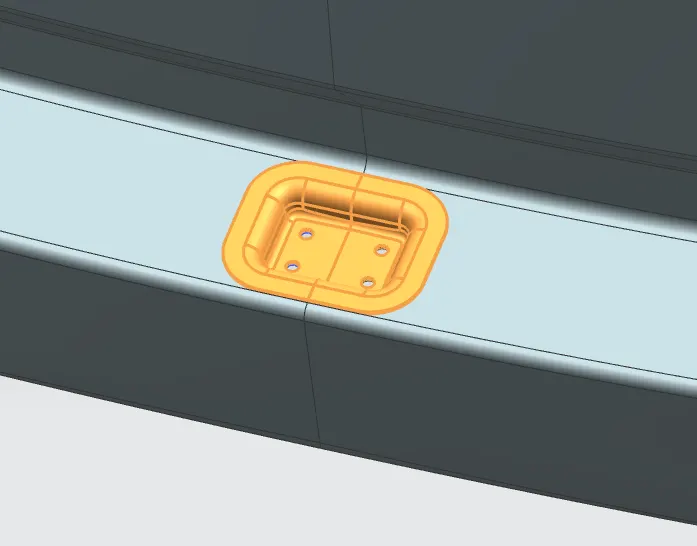
Wiper Motor Reinforcement:
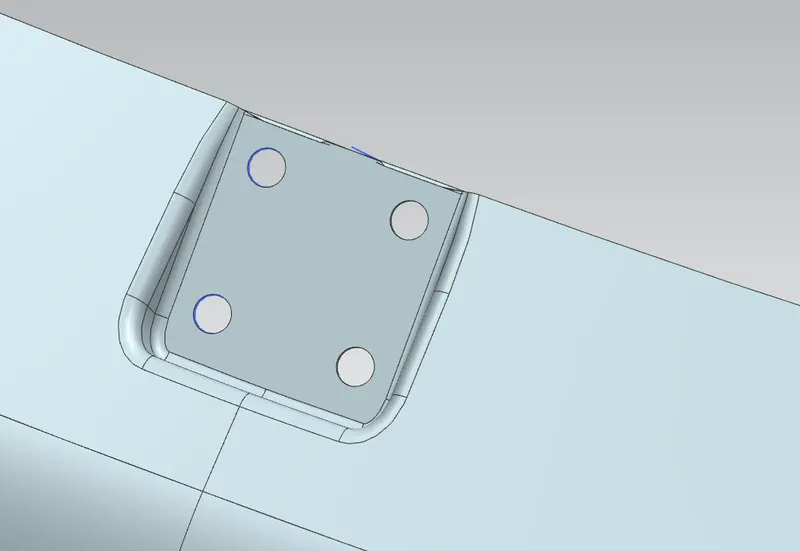
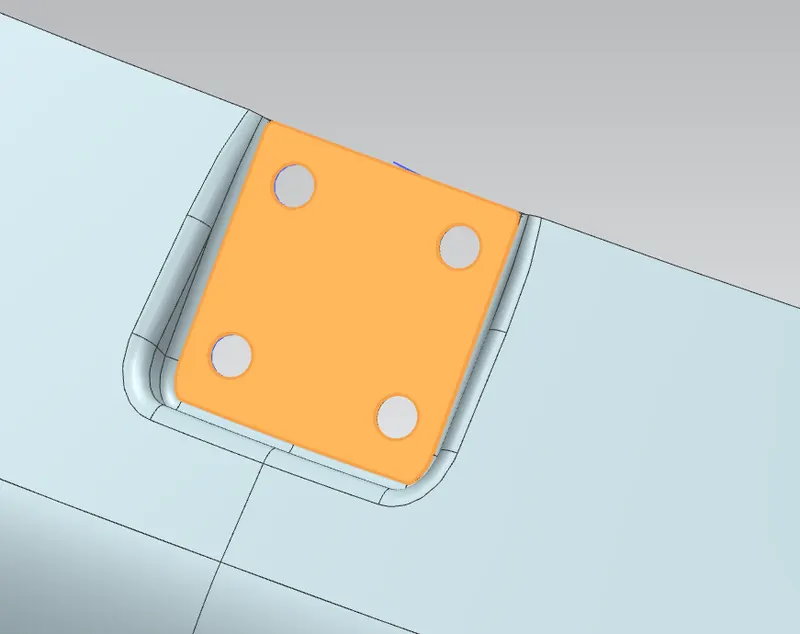
Hemming:
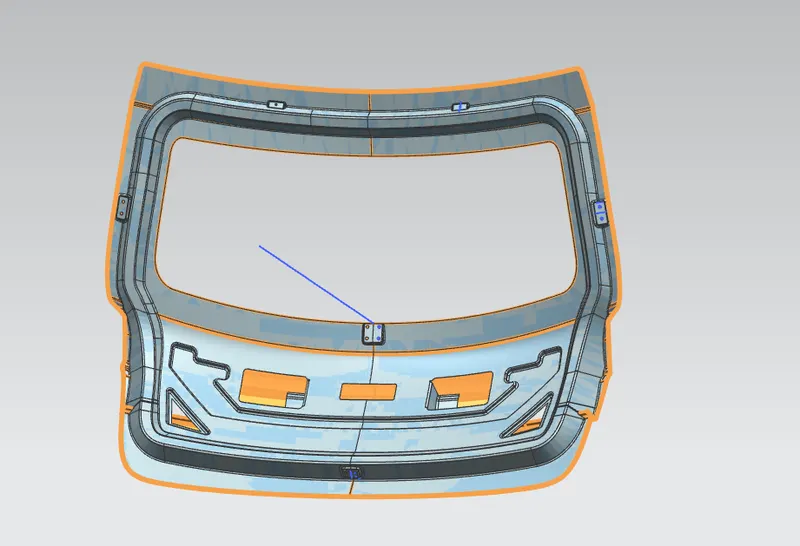
Assembly:
 *******
 ******
 *******
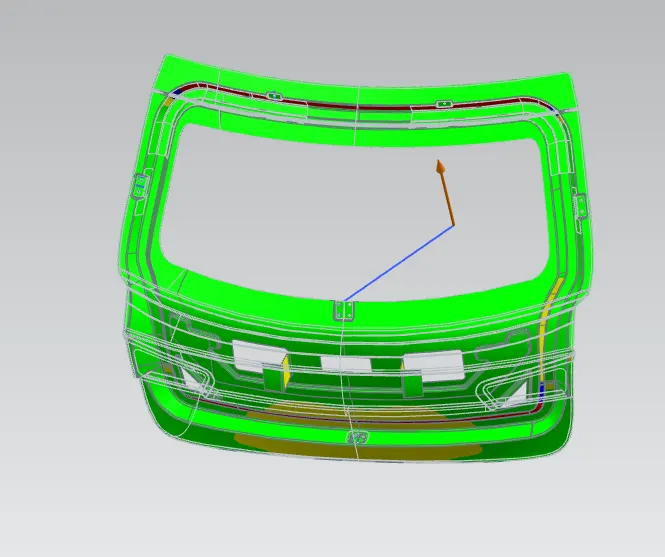
Draft Analysis:
 *******
CONCLUSION
The back door outer and inner panel were designed with the help of the styling surface along the tooling direction and
Draft analysis was performed on the inner panel and all the reinforcements were designed and placed at approprite positions.