Design of backdoor
AIM:
Use the provided styling surface to come up with a back door design, use appropriate design methodologies, and provide the necessary reinforcements and embosses.
INTRODUCTION:
The trunk (North American English) or boot (British English) of a car is the vehicle's main storage or cargo compartment, often a hatch at the rear of the vehicle. It is also called a tailgate. These doors can be operated manually or electric powered. In most luxury cars door is electrically operated. It involves a very major role during rear crash cases. So our design must obey crash requirements. The institute of highway safety analyses the different accidents and they set a test to rate our car. So these ratings depend upon the design of the trunk and material used, flanges, embosses, type of joining of the inner panel and outer panel, etc.
The total no. of the parts in Backdoor are:
- Back door outer panel (upper)
- Back door outer panel (lower)
- Back door inner panel
- Hinge reinforcements
- Gas stay reinforcements
- Latch and striker reinforcements
- Wiper motor reinforcements
Inner Panel
The inner panel, as the name suggests, is the inner part of the door. This is where most of the reinforcements and components are mounted. It is manufactured either by casting (aluminum) or sheet metal stamping (steel). The thickness of the inner panel is 0.75 mm.
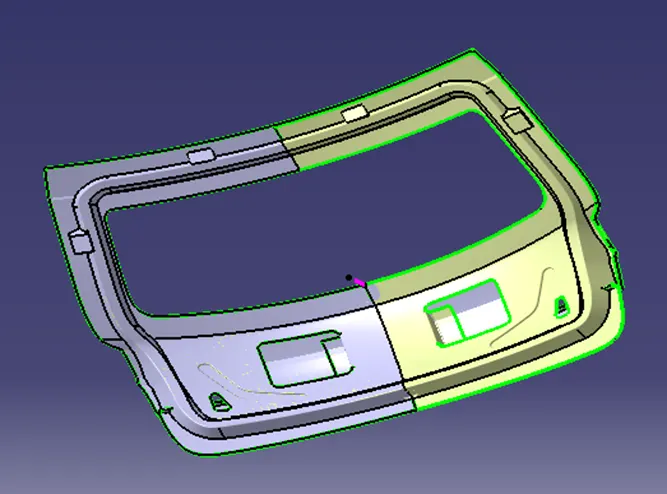
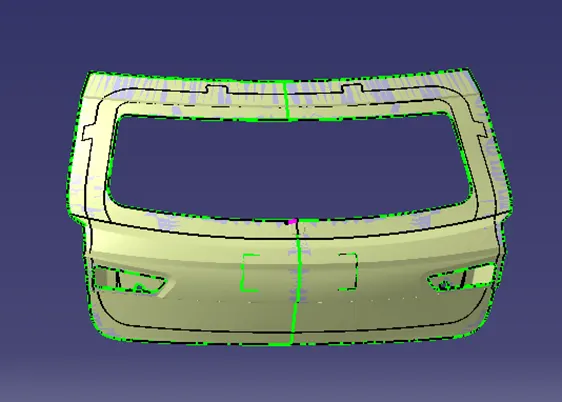
Outer Panel
As the name suggests, it is the outer part of the rear door and is mostly responsible for the aesthetics of the vehicle. Outer and inner panels are connected by mastic sealants in the center and by a hemming process at the edges. The outer door handles and in some cases, the number plate may also be installed on the outer panel of the back door. We have considered a 2-part outer panel for our design, outer upper panel and outer lower panel prospectively. The outer panel is manufactured by stamping sheet metal. The thickness of the outer panel is 0.75 mm.
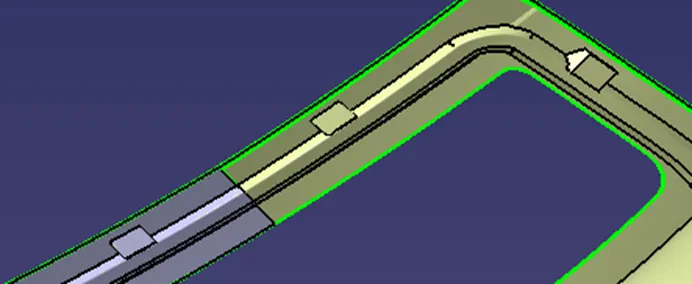
Reinforcements
Reinforcements are provided to provide support and add extra material to the sheet metal part to increase its strength near component installation regions and minimize the impact of collisions. We have considered the following reinforcements during our design. The reinforcements may be manufactured by stamping. The thickness of all reinforcements is 1.5 mm.
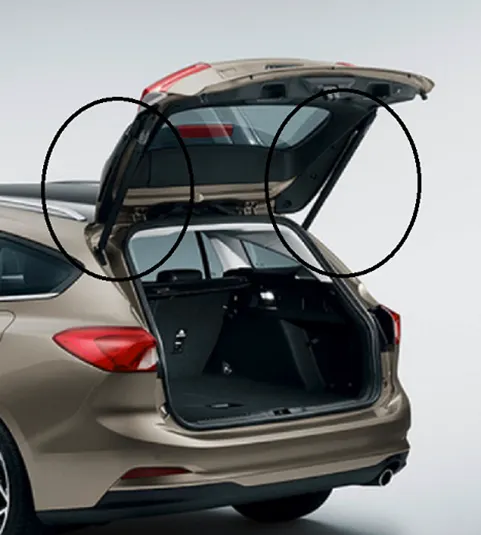
Gas Stay
Gas stay is basically a gas spring that relies on the elastic deformation of a compressed gas that is enclosed in a cylinder. It is used to reduce the required effort while opening the back door. Although all the cars don’t come with gas stays, it may be required in case of a heavy back door.
Wiper and wiper motor mounting
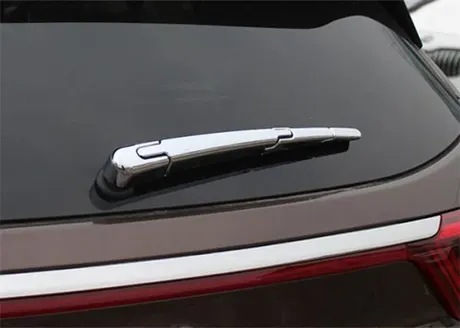
As the name suggests, a wiper is used to wipe off dust and water from the rear windscreen of the vehicle.
Design Methodology:
We start with the styling surface that is provided to us and consider a top-down approach for this assembly modeling. First, we create the assembly and then create the components in the assembly file itself. Inner and outer panels are the largest parts and all other parts depend on them so we start with them. Also, the given styling surface is part of the outer panel so we created it first. Using various commands and features, we design the outer panel from the styling surface. We have 2 parts for the outer panel, which are separated by a flange, hence we create an outer panel upper and lower respectively. They will be spot welded with each other. It is necessary to make sure that all the surfaces are properly jointed to their adjacent surface and that there are no disjoints at their intersection edges to avoid further errors. Also, the Inner and Outer panels are connected through the hemming process so we can go back to the outer panel and do that after completion of the inner panel.
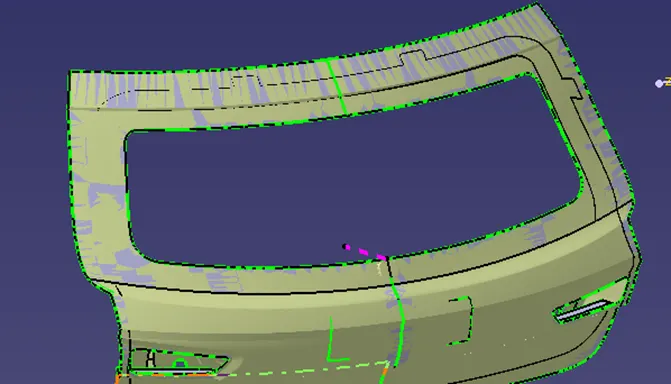
Now, as we know the inner panel is at a particular distance from the outer panel, we offset the outer panel surface and design the inner panel on the same. The inner panel is important as most of the mountings will be done on it. Before starting the inner panel design, we need to define the tooling direction as a reference for the manufacturing team. Then we design the inner panel.
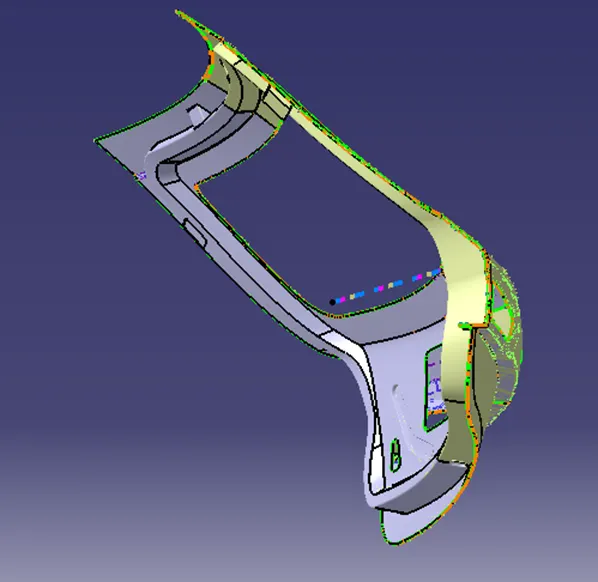
While designing the inner panel we need to consider various factors like the mounting point positions, mastic sealant application positions, and the cutouts in the sheet to make access to tail light assembly easier. As the bottom center part of the inner panel is not connected to the outer panel, we need to create a surface that comes out and connects to the outer panel as shown in the image. This part will be connected to the outer panel using mastic sealant. Also, the hinge embosses must be taken by considering proper directions. The emboss surface must be parallel to the z-axis to get proper geometry for the latch striker path curve. Then we draw a line connecting the hinges, such that it forms the hinge axis (axis around which the door rotates while opening or closing). Then we can draw a circle with the center at the hinge axis and circumference passing somewhere around the embossed endcap. So when we get the emboss for latch striker mounting, we can take the end cap by creating a plane normal to the path (using On Curve) in the direction normal to the path of the striker. Thus, after some trial and error, we can adjust the emboss and the circle dimensions properly.
Different types of Sheet metal operations are done in the Back Door
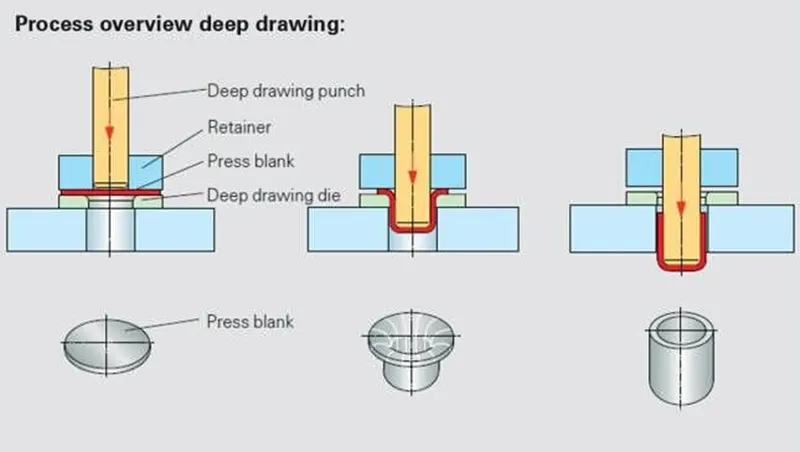
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing cups, cans, and other similar deep drawing products. Deep drawings have two main categories.
First-stage drawing: The blank shape of metal is placed on the die and in contact with the punch. When the metal specimen is a flat piece of sheet metal is used in forming and finishing the product. Initially, the punch moves in a downward direction. The outer rim of the blank is subjected to pure radial drawing (drawing toward vertical axes) between the die and blank metal. The metal becomes a bend and slides over the die and also stretches between the die and punch. The metal in the vicinity of the punch head and contact with it bends and slides over radii and stretches over the punch head.
Redrawing: The components drawn from the first stage are again redrawn and converted into more depth to form a cup shape in the die and punch. The second stage of drawing is called redrawing.
Embossing:
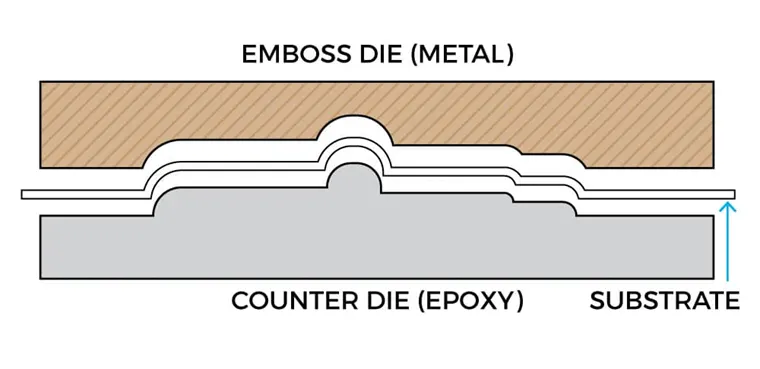
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. The metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum Alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
Hemming:
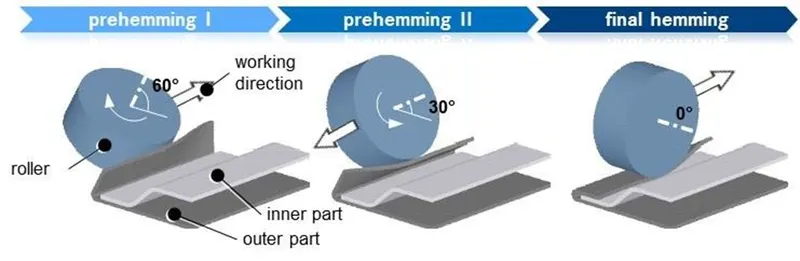
- Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, improve the appearance of a part, and reinforce part edges.
- In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming, and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids, and fenders.
There are various types of hemming operations:
- Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
- Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
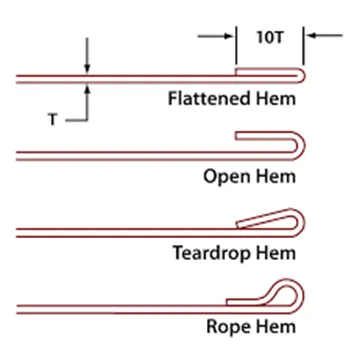
- Open Hem: A Hem has a full round feature and a return flange. In an open hem, the bend angle is equal to 180 degrees.
- Teardrop Hem: In teardrop hem, the bend angle is greater than 180 degrees.
- Closed Hems: Hems without any inside radius are called closed hems. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
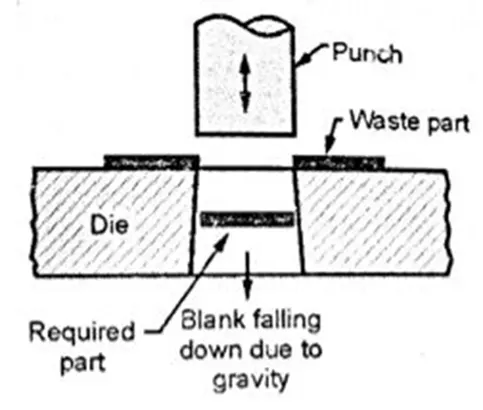
Blanking:
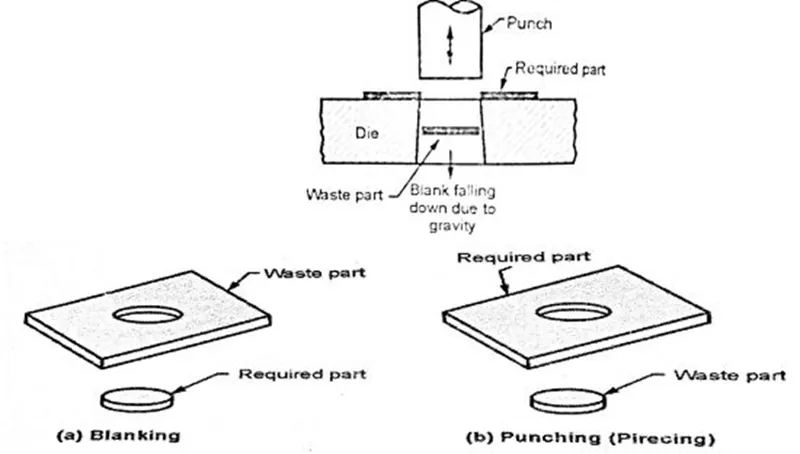
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered a waste.
Punching:
It is similar to blanking only the main difference is that the hole is the required product and the material punched out from the hole is considered a waste.
Inputs for designing the backdoor:
Outer Panel - 0.75 mm
Inner Panel - 0.75 mm
Reinforcements - 1.5 mm
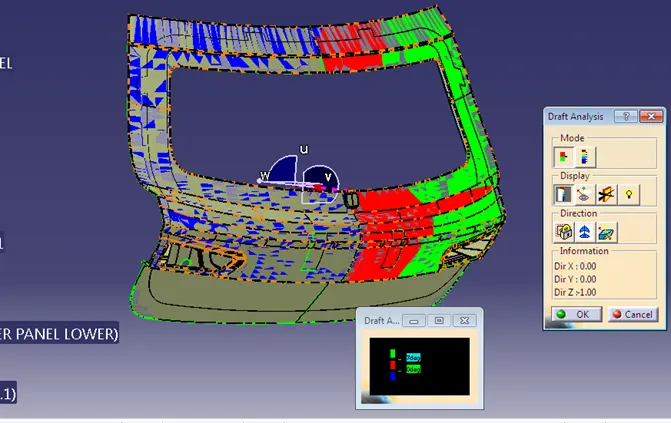
Draft analysis: In order to make sure the drawing of the inner panel body is proper; we do a draft analysis. We need to define the drawing direction and select the inner panel body. We take the limit angle as 7 degrees. The results of the draft analysis are as follows,
CONCLUSION
The back door outer and inner panel was designed with the help of the styling surface along the tooling direction. Draft analysis was performed on the inner panel and all the reinforcements were designed and placed at appropriate positions.