Design of backdoor
Aim:
To design car back door from given styling surface data under given design rules and regulations.
Objective:
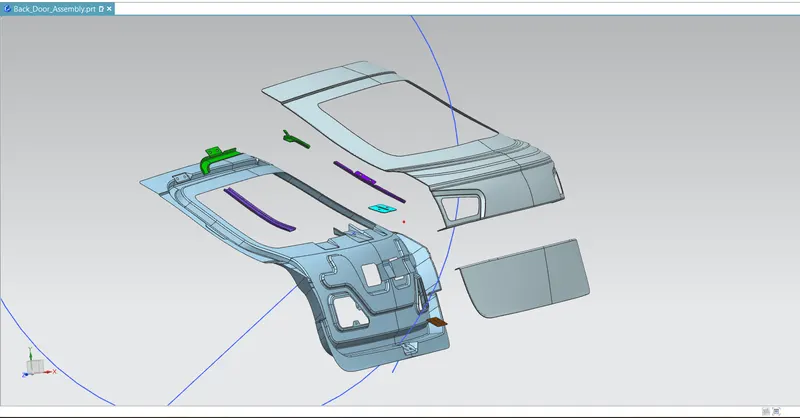
- The objective of this project is to design a BIW Back Door of a car with an Inner Panel, Outer Panel, and Reinforcements for the Hinges, Gas stay, Wiper Motor, and Latch by following the engineering standards.
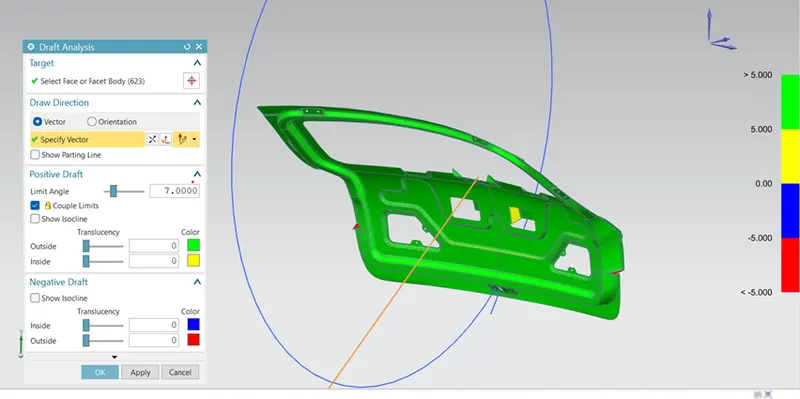
- The Inner Panel must be subjected to Draft Analysis for verifying whether it satisfies the Deep Drawing requirements for the tooling direction created in the design.
Introduction:
The Back Door of a car is the rearmost part of the vehicle which gives access to the trunk space of the vehicle. The rear door also supports the reinforcements and added weights of the Wiper Motor, Gas Stay, Tail Lamp, and Latch and Striker.
The Backdoor/tailgate is one of the closure commodities in BIW sheet metal design. The backdoor has a lot of components inside and is designed to incorporate them easily. It affects the rear visibility and luggage area.
The material used for door manufacturing depends on the budget and performance of the vehicle. Mostly Aluminium and Steel will be used whereas low-budget vehicles use Steel which makes the manufacturing process easy and cost-efficient since it follows the Stamping of Moulds.
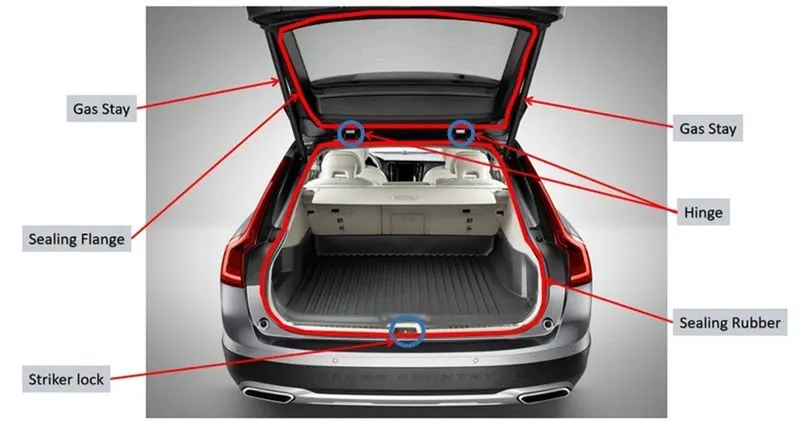
Design Considerations for Back Door:
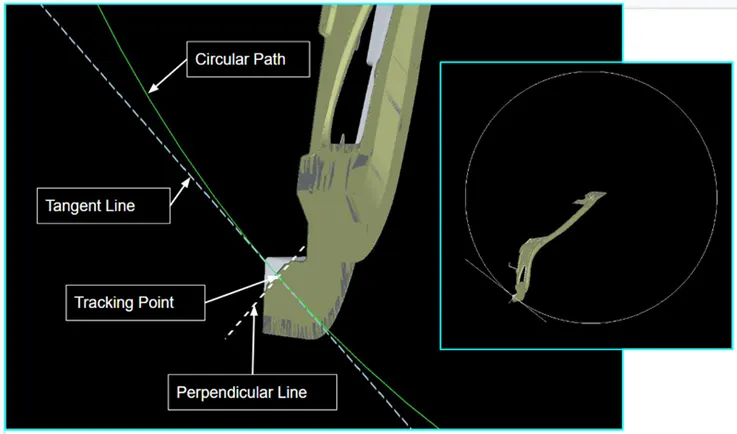
Striker Position:
The position of the hinge should be perpendicular to the latch when the latch and striker meets. for that, a circle is drawn from the center of hinge axis to find the path of the striker. and positioned it perpendicular to the path.
Rear visibility criteria:
Federal motor vehicle safety standard (FMVSS) No. 111, “Rear Visibility,” currently requires that vehicles be equipped with rearview mirrors to provide drivers with a view of objects that are to their side and rear.
Gap and flushness requirement:
Mastic Seals:
Mastic Seals place b/w Inner and outer panel to reduce noise, vibration, and harshness. Every Mastic will have an effect of 80mm Dia. The inner and outer panel gap is 4 to 5mm. 0.2mm gap is required for the Hemming and that gap will be filled by sealed past.
Adding reinforcements and stiffener pad:
reinforcements are added were and all the weight is added. On the inner panel, we have Hinges and striker, which are attached to the inner panel so due to this attachment the strength of the inner panel is going weak. In order to strengthen the inner panel reinforcements will play a very important role. A stiffener pad is a sponge-like material place b/w Inner and outer panel to reduce vibrations.
Different type of sheet metal operations done in back door:
Deep Drawing:
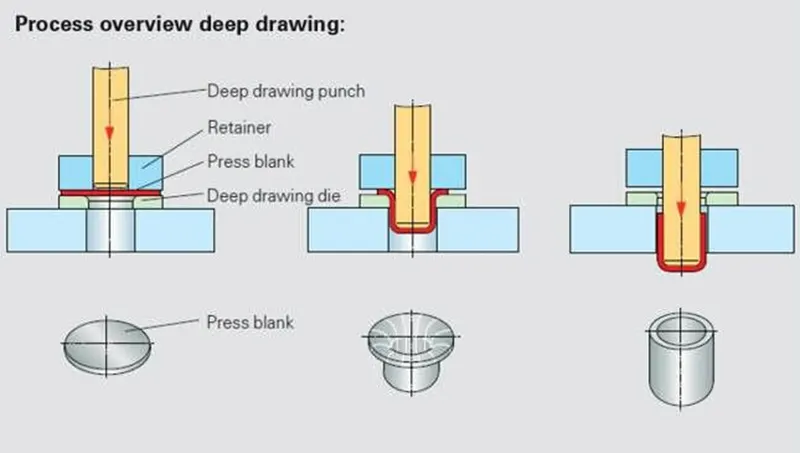
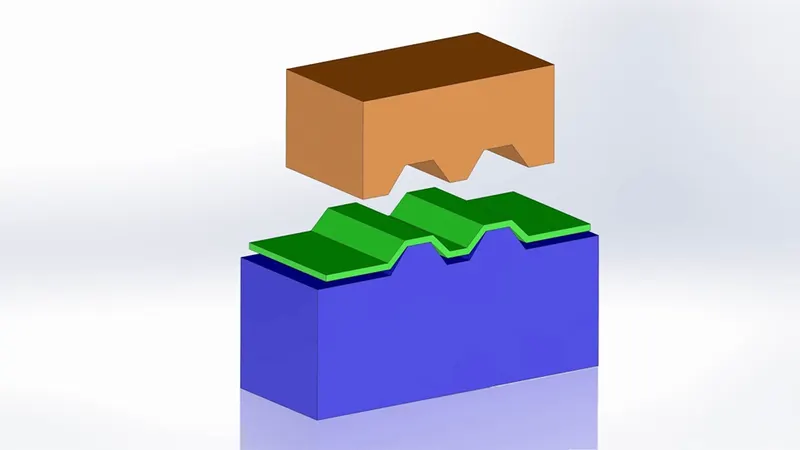
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
First- stage drawing:
The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
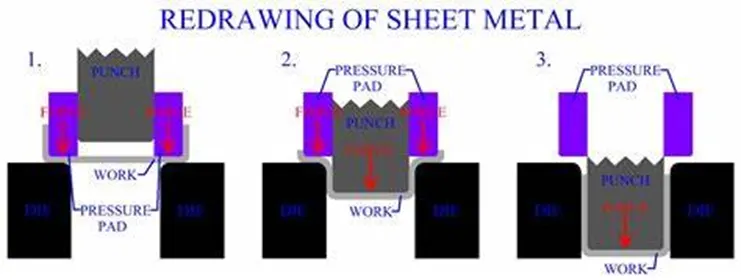
Redrawing:
The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
Hemming:
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
There are various types of hemming operations:
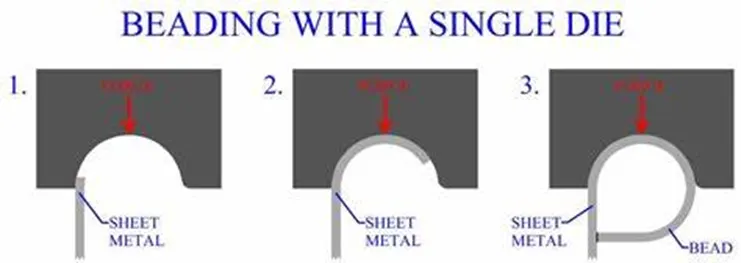
- Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
-
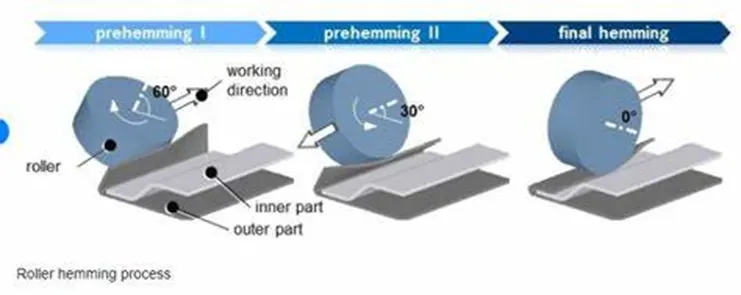
Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
-
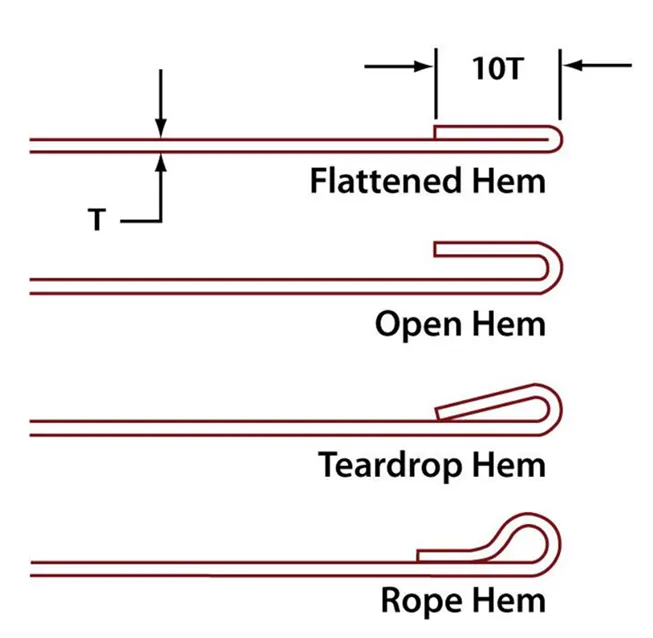
Open Hem: A Hem has a full round feature and a return flange. In open hem bend angle is equal to 180 degrees.
-
Tear drop Hem: In tear drop hem the bend angle is greater than 180 degrees.
-
Closed Hem: Hems without any inside radius are called as closed hem. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
Blanking:
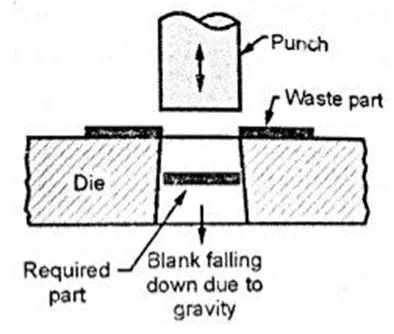
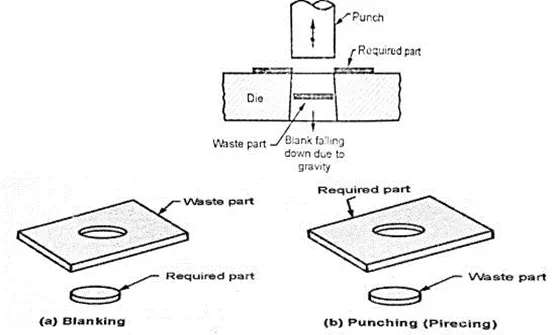
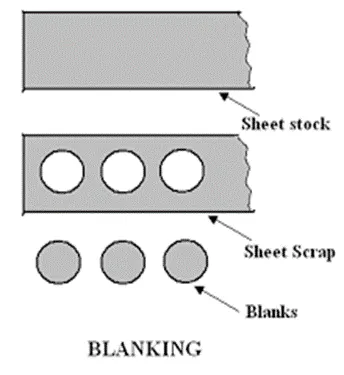
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered as a waste.
Punching:
It is similar to blanking only the main difference is that, the hole is the required product and the material punched out from the hole is considered as a waste.
Emboss definition:
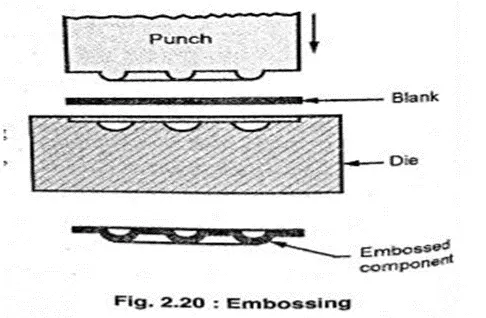
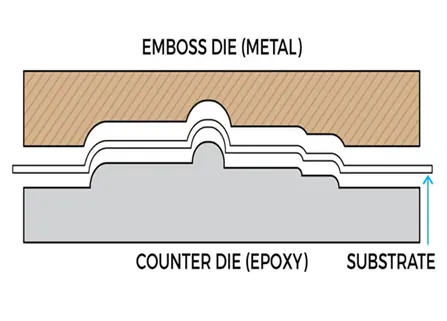
Embossing is a forming process in which a high pressure is applied to a workpiece to change its surface. Depending on the shape, a distinction is made between hollow embossing and solid embossing.
Embossing:
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled stee
Back door Component:
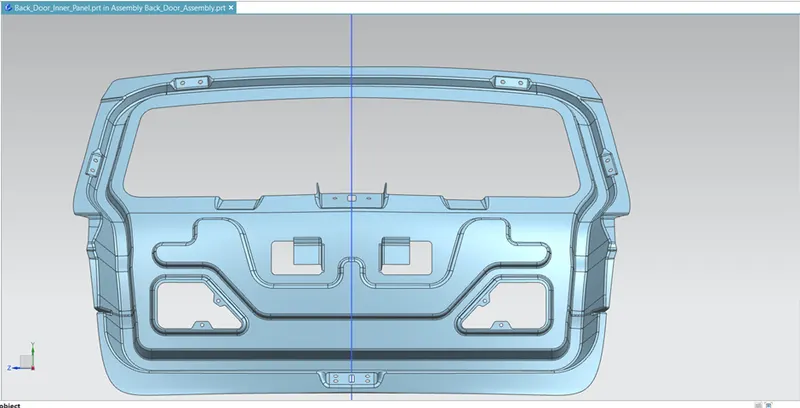
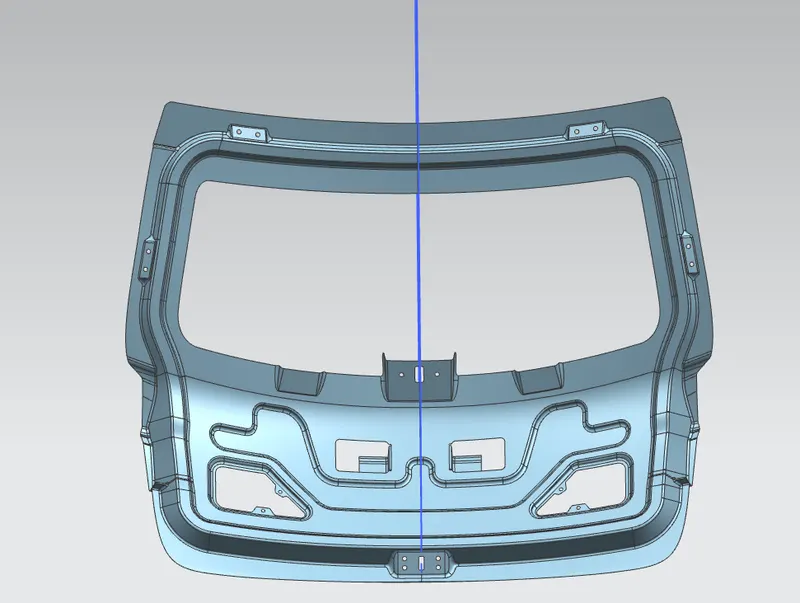
Inner Panel:
The inner panel, as the name suggests, is the inner part of the door. It is where most of the reinforcements and components are mounted. It is manufactured either by casting (aluminum) or sheet metal stamping (steel). Thickness of inner panel is 0.75 mm.
Outer Panel:
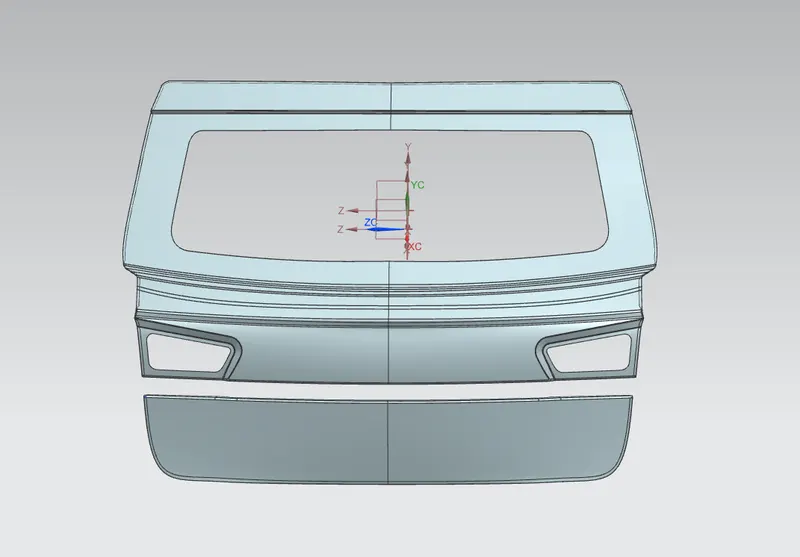
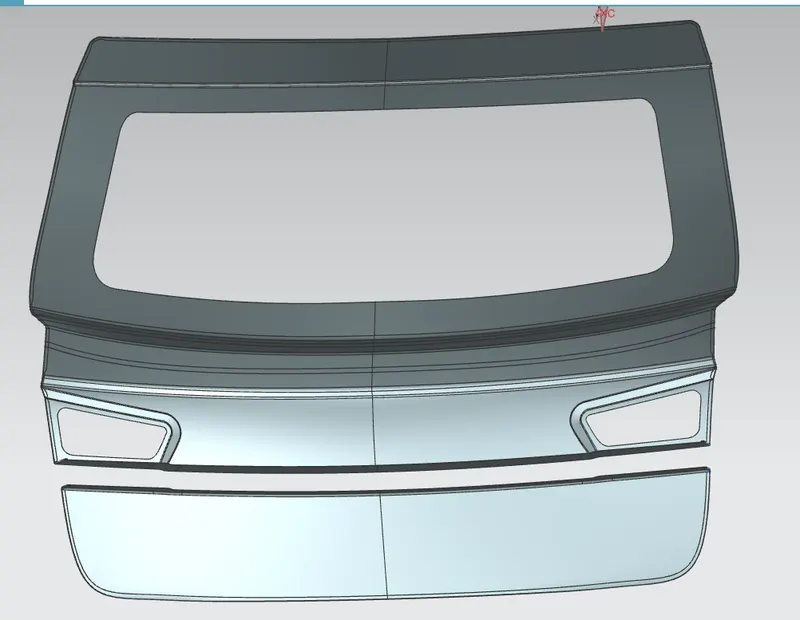
As the name suggests, it is the outer part of the rear door and is mostly responsible for aesthetics of the vehicle. Outer and inner panels are connected by mastic sealants in center and by hemming process at edges. The outer door handle and in some cases, the number plate may also be installed on the outer panel of the back door. We have considered a 2-part outer panel for our design, outer upper panel and outer lower panel prospectively. Outer panel is manufacture by stamping sheet metal. Thickness for outer panel is 0.75 mm
Reinforcements:
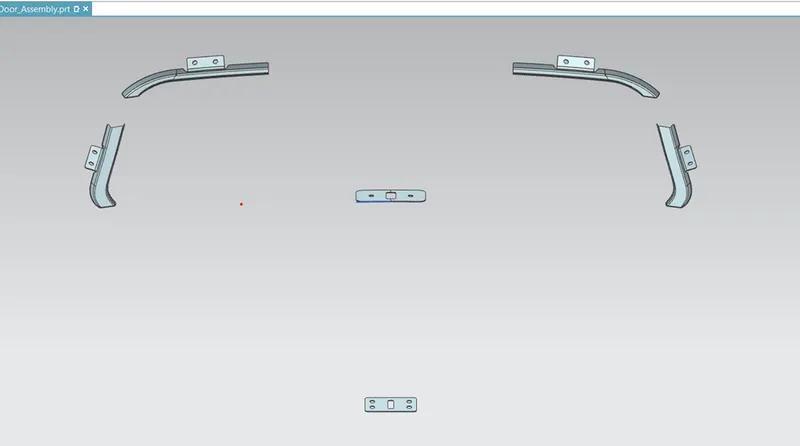
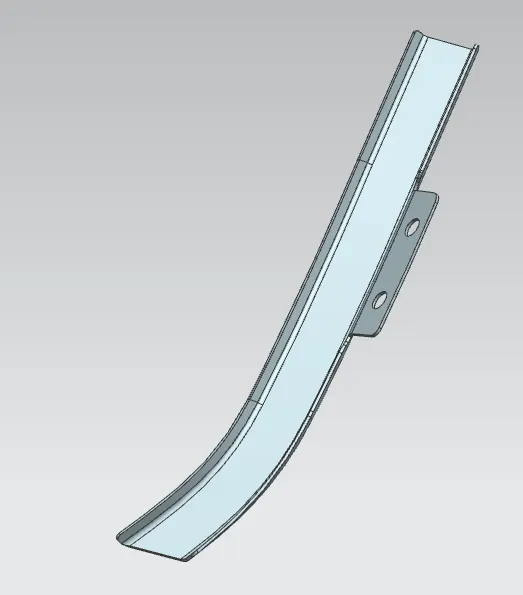
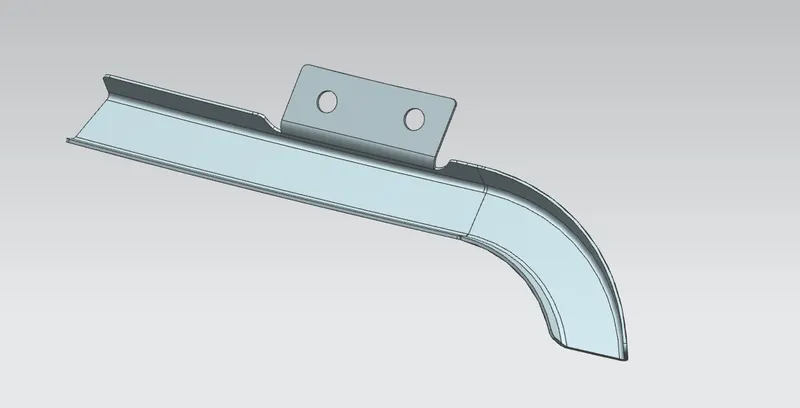
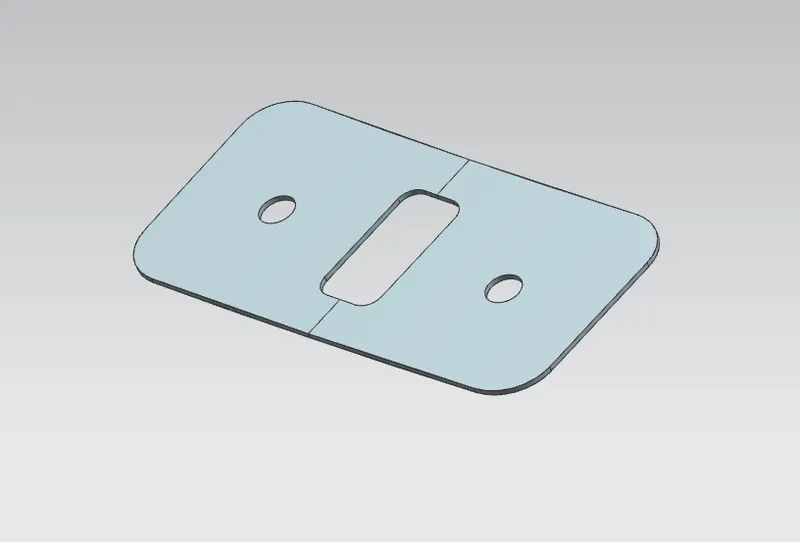
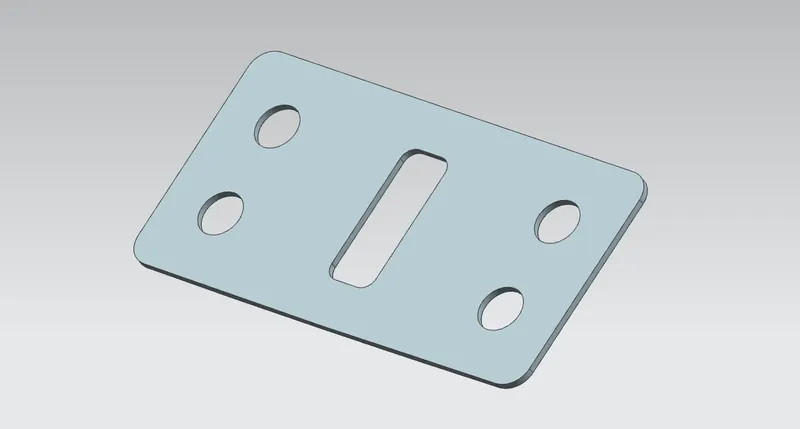
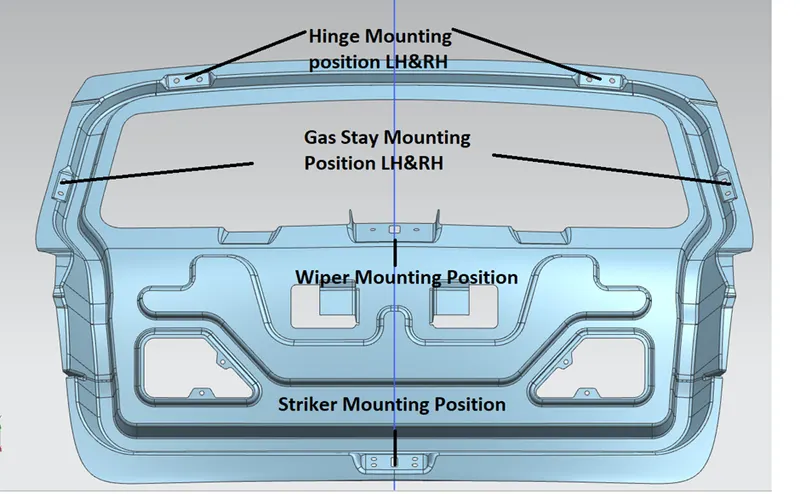
Reinforcements are provided to provide support and add extra material to the sheet metal part to increase its strength near component installation regions and minimize the impact of collisions. We have considered following reinforcements during our design. The reinforcements maybe manufactured by stamping. Thickness of all reinforcements is 1.5 mm.
Gas Stay:
Gas stay is basically a gas spring that relies on elastic deformation of a compressed gas which is enclosed in a cylinder. It is used to reduce required effort while opening the back door. Although all the cars don’t come with gas stays, it may be required in case of a heavy back door.
Wiper and wiper motor:
As the name suggests, wiper is used to wipe off the dust and water from the rear windscreen of the vehicle.
Hinges:
Hinges connect the door with the vehicle body and allow the door to rotate around a fixed axis for opening and closing movement. Generally, hinges are a 2-part assembly, where one part is bolted to door and other is bolted to vehicle body.
Tooling Direction:
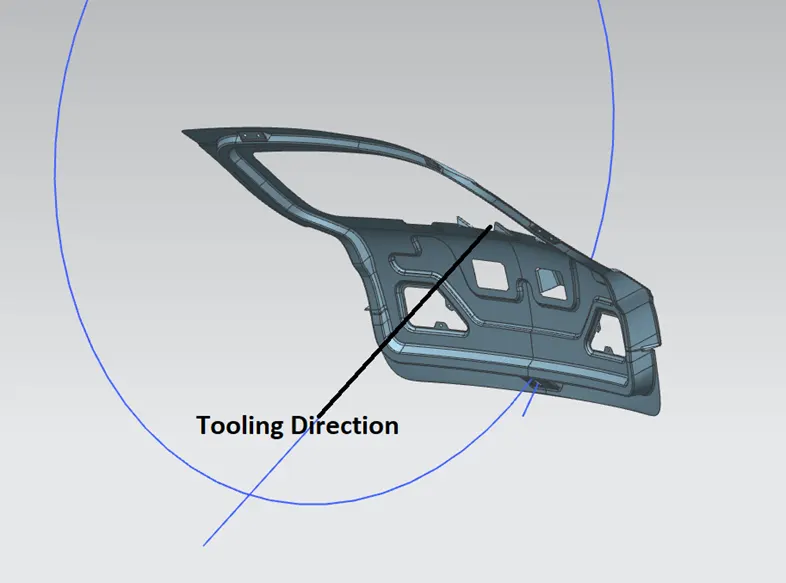
Before starting to design the inner panel of the back door the tooling direction for Deep Drawing purpose should be created.
Then the styling surface needs to be checked and analyzed since it might have irregularities, hence it must be fixed first.
Then the back door was designed using the top-down approach.
The Tooling Direction for the inner panel is derived using bisection lines of the part from two sides.
In part design, use a thick surface option to make a sheet, here 0.75mm is the thickness of the inner panel.
Draft Analysis:
Draft analysis is a method of checking the draft angle on various faces of a part with a particular direction.
It should be more than 7 deg for aluminum for hard metals, min draft angle is 10 deg.
This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
Conclusion:
Thus the back door was designed from the given styling surface and Draft analysis is also done on the inner panel to check the manufacturing conditions.