Design of backdoor
Aim:-
To design the back door using the given styling surface.
INTRODUCTION:-
The back door or till gate is the real most part of the automobile which open upwards downwards and sideways to give access to the luggage base or seatings full stop in most automobiles the back door opens upward it is hinched to the roof and a gas stay Support fixed at the body side outer for keeping the back door in the open position.
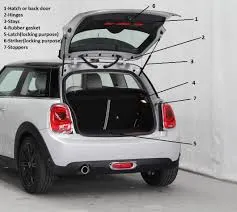
Top mounted back door of the car
The material used in making the back door of the car is mainly Steel but nowadays Aluminium is also used in making the panels.
The main advantage of Aluminium is that the density of Aluminium is very less as compared to Steel so it is reduced the overall weight of the car. But Aluminium is more costly as compared to Steel.
TYPES OF DOOR OPENNING:-
- Top mounted door
- Side mounted door
- Bottom door
Different processes used for manufacturing the back door are
The metal deep drawing process is an effective method of manufacturing cups, cans and other similar deep drawing products. The deep drawing having two main categories.
1) First stage drawing:-
The blank shape of metal is placed on a die and in contact with the punch. When the metals specimen is a flat piece of sheet metal is used in farming and finished the product. Initially, the punch moves in a download direction. The outer ring of the blank is subjected to pure radial drawing between the die and the blank metal. The metal becomes a bend and slides over the die and is also stretched between dye and punch. The metal in the vicinity of the punch head and contact with it bend and slide over the radii and stress over the punch head.
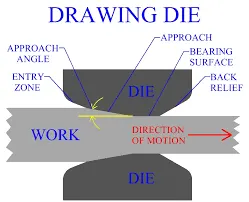
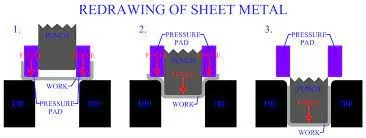
2) Redrawing:-
The components drawn from the first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called redrawing.
Hemming:-
The inner and outer panels are joined by the process of hemming.
Hemming is a forming operation in which the edges of the sheet are folded over the other parts in order to achieve a tight feet usually, hemming operations are used to connect parts together to improve the appearance of the part and to reinforce parts edges.
In car park production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operation to join two sheet metal parts together. Typical parts for this type of assembly are hoods, doors, trunk lids and fendors.
The accuracy of the heming operation is very important since it affects the appearance of the surface and surface quality. Material deformations which occurs well the heming process, can lead to dimensional variations and other defects in parts. Typical heming defects are splits and wrinkles in the plants material overlapse in the corner areas. So it is very important to use simulation software tools to better understanding the hamming process and minimise the number of trials and error during the try out.
There are different types of hemming operations:-
Conventional die hemming:-
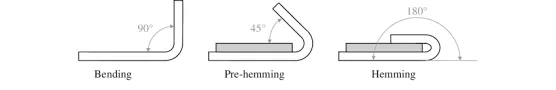
In conventional die hemming, the flanch is folded over the total length with a hemming tool.
Roller hemming:-
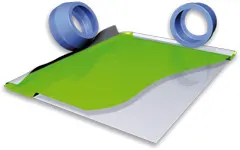
In roll hamming, roller is carried by an industrial robot to make the flange.
COMPONENTS OF BACK DOOR:--
- Inner panel
- Outer panel
- Hinge reinforcement
- Gas stay reinforcement
- Wiper motor reinforcement
- Latch and striker reinforcement
Design considerations of a backdoor:
- Functional requirements of hinge and gas stay
- Rear visibility criteria
- Luggage volume area
- Crash analysis
- Bend test, dent test, toraion teat and endurance test
- Rear crash regulation
- Gap and flushness requirement
DESIGN OF BACKDOOR
The outer panel is a styling surface of the back door design. Other components of the back door are designed with reference to the outer panel surface. IT act as the outer cover and deals with the aesthetics of the car.
In designing the outer panel is divided into two parts they are
- Outer upper pannel
- Outer lower panel
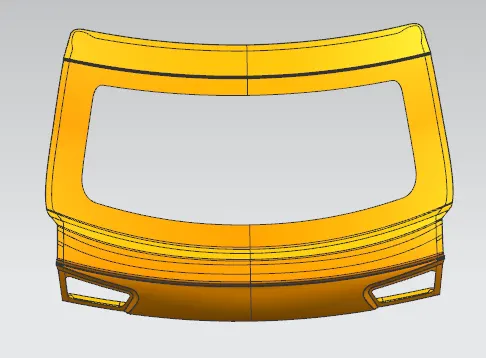
Outer upper panel:-
The outer upper panel extracted from is providing styling surface. The panel is modified for the required design with the surface tools of NX CAD.
The thickness provided to the outer panel is 0.75 mm. Hemming his provided with the corner relief.
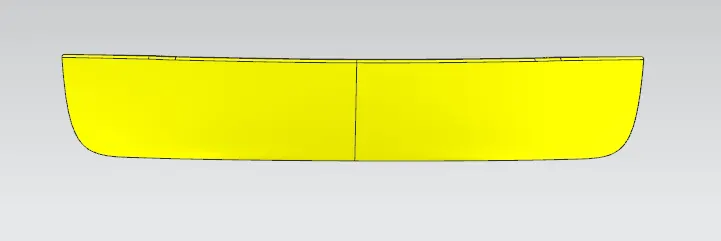
Outer lower panel:-
The outer upper panel extracted from is providing styling surface. The panel is modified for the required design with the surface tools of NX CAD.
The thickness provided to the outer panel is 0.75 mm. Hemming his provided with the corner relief.
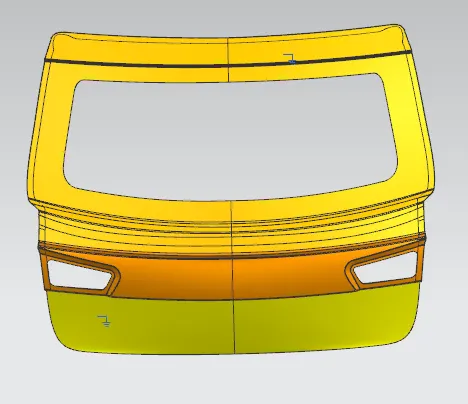
Outer upper and lower panel
Tooling direction:-
- Before starting to design the inner panel of the back door the tooling direction for deep drawing purposes should be created.
- Then the styling surface needs to be checked properly and analysed since it might have irregularities has it must be fixed first.
- The back door was designed using a top down approach.
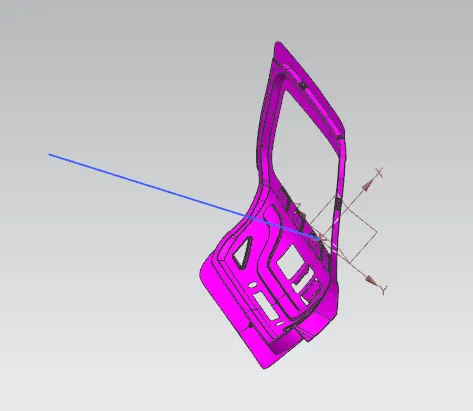
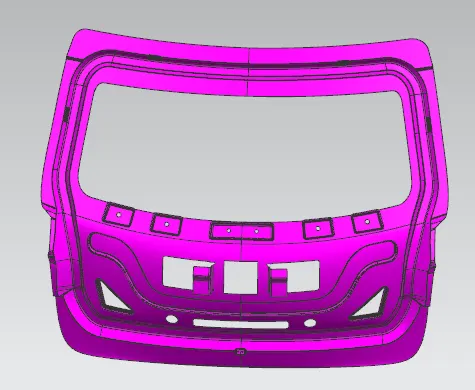
Design of back door inner panel:-
The inner panel extracted from is providing styling surface. The panel is modified for the required design with the surface tools of NX CAD.
The thickness provided to the outer panel is 0.75 mm.
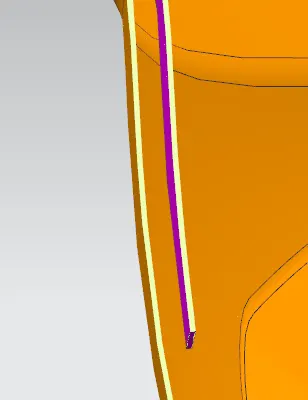
Mastic sealant:-
Domestic sealant is used to fix the inner panel and the outer panel which increases the NVH factor and stiffness of the back door.
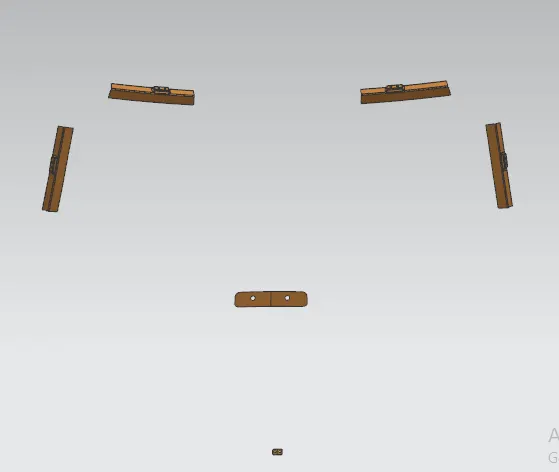
HINGES, GAS STAY, WIPER MOTOR & LATCH AND STRIKER EMBOSSES:
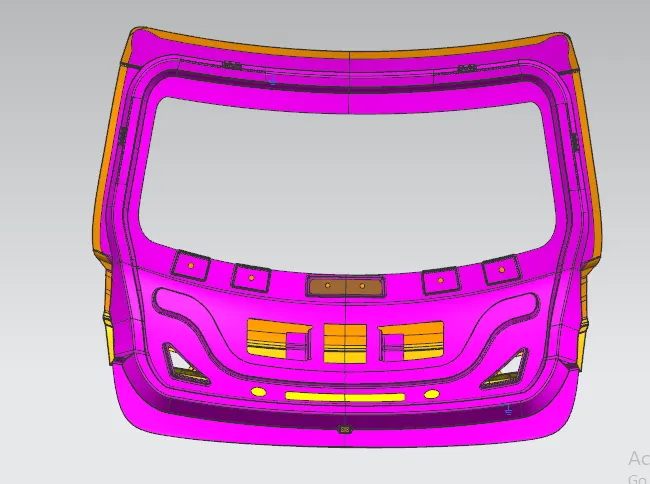
The green circle denotes the hint emboss which was created using the determ plane and emboss feature in annex full stop it is also designed in a way that the emboss should have a flat surface for assembling the hing using it the blue circle denotes the gas day and Boss which was created using the surface of the connecting plans. The orange circle denotes the wiper motor emboss which was created using the surface of the connecting plans the yellow circle denotes large and striker and watches where designed by creating a trajectory that follows the opening and closing of the back door with respect to access of the Hinges.
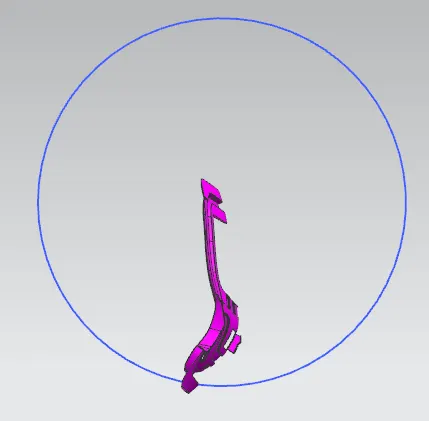
Trajectory:-
The position of the hing should be perpendicular to the large at the time of large and strikermates. The circle is drawn from the centre of the hing access to find the path of the striker and perpendicular to the path.
Hemming:-
Hemming and seaming are two similar types of metal working process in which a sheet metal edge is rolled over into itself.
- The outer panel was designed as two different parts named as outer upper panel and outer lower panel.
- After designing the outer panel the hamming was created by offsetting the surface with the help of face blend and Sweft volume.
- The two different outer panels will be joined using blanking.
Corner relief:-
During the hemming process, when giving the corner relief helps to control sheet metal material behaviour and to prevent the unwanted deformation during unbend operations and also help to minimise the number of passes in hemming.
DESIGNING THE REINFORCEMENT:-
HINGE REINFORCEMENT:-
Hinges allow the opening and closing of the back door. One end of the hinge is fixed on the back door and the other and on the roof. In just can be placed outside or inside the back door.
The hing reinforcements are added to compensate for the week reason due to the acting load over it.
GAS STAY REINFORCEMENT:-
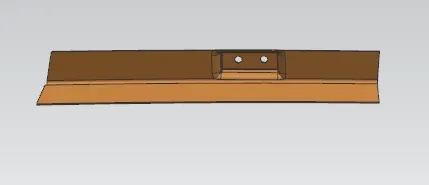
Gas stay is device used to support the back door in its open position. Gas stay requires no manpower and it is engaged into support position automatically as the back door opens. One end of the gas stay is fixed on the back door and another and is on the body side or on the back door stationery area.
Embossing is provided at the gas day mounting area to compensate for weakness and improve strength.
WIPER MOTOR REINFORCEMENT:-
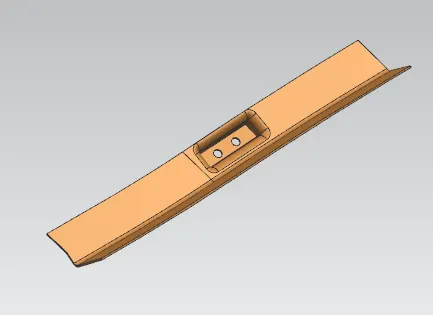
Wiper motor reinforcement is made to mount the wiper motor assembly.
LATCH AND STRIKER REINFORCEMENT:-
Latch and striker together from the locking mechanism of the back door with the car. Due to regular opening, closing and over slamming of the back door there is stressed developed in the large and striker area. To recoup for the same reinforcements are added in the area.
DRAFT ANALYSIS:-
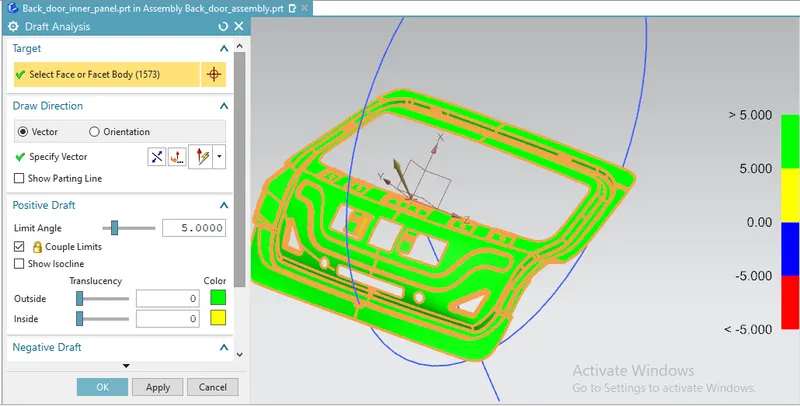
- Draft analysis was performed for the tooling direction created at first and checked that the model is suitable for manufacturing.
- Then to get a complete green portion required changes to the draft angle of the embosses were carried out by optimising the model.
- The draft analysis command is used to detect that the part drafted will be easily removed or not
- This type of draft analysis is performed based on colour ranges.
- The identifying zones on the analysed element where the deviation from the draft direction at any point, corresponds to specified values.
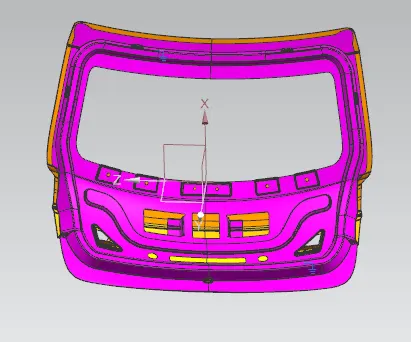
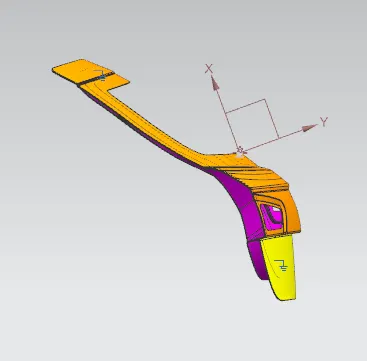
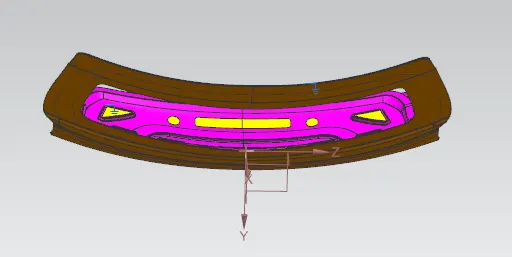
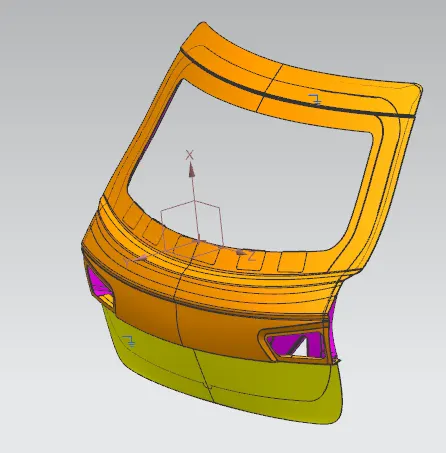
View of the back door design:-
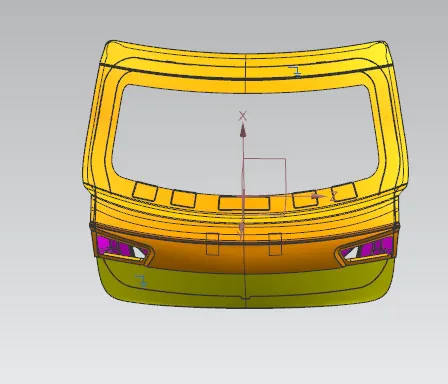
FRONT VIEW:-
BACK VIEW:-
SIDE VIEW:-
TOP VIEW:-
ISOMETRIC VIEW:-
CONCLUSION:-
Does the body in the white back door of a car was designed by the following engineering standards and also the deep drawing requirements consideration.