Week 9 - Project 1 - Door Trim Lower with Engineering Features
Door Trim - Engineering Features
Aim :
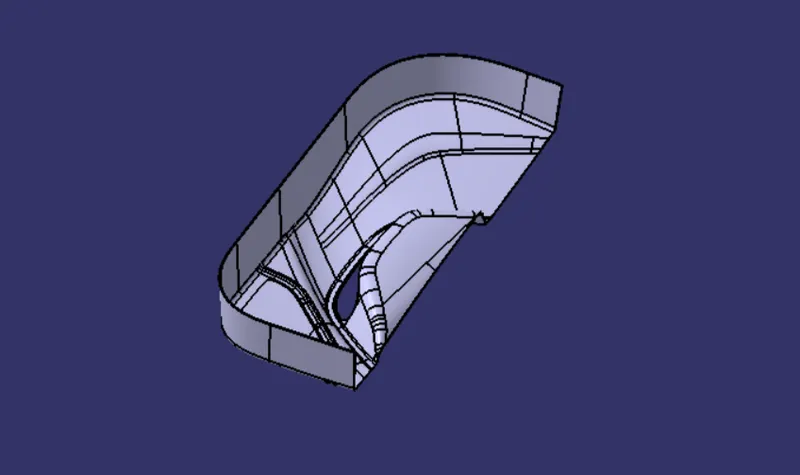
To create the Door trim lower plastic component through the given Class-A surface and attach the engineering features such as Locaters and Heat stakes and perform the Draft analysis.
Objective :
- Create the Tooling axis by using the bisecting method.
- Design the class-B and class-C surface and join them.
- Create the solid feature by surfaces we create.
- Design the required Ribs and Screw Boss and analysis them.
- Perform the Draft analysis for the final component.
Theory :
Tooling Axis :
Class-A surface is first analyzed to create the tooling axis or tooling direction that molds pull apart in injection molding. Tooling direction is important for plastic product design as it decides direction for mold seperation.
Step followed for creation of tooling axis :
- Reference point is first created on extracted surface.
- New axis system is deployed to plot clearance lines.
- The X-direction and Y-direction along the class-A were used to create tooling axis.
- Graphic properties of tooling axis were change before publishing.
Draft Analysis :
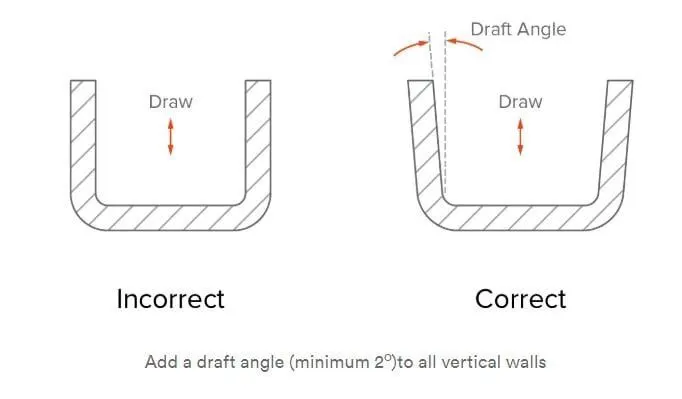
The Draft angle is the amount of taper for molded or cast parts perpendicular to the parting line. It can be measured in degrees. A functional part for injection molding has to have Drafts facing both cavity and core sides to reduce the risk of damage to the parts and ensure ejection. And also important is to overcome the vaccume forces by letting air in between the metal to the plastic for the part to relaese properly. Adding maintaining a decent cosmetic finish.
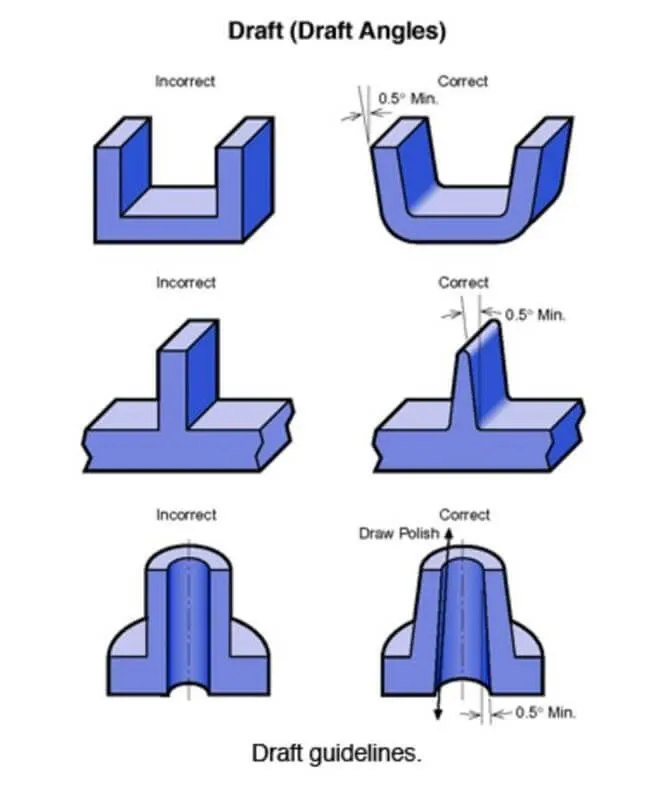
Draft should be a part of design for manufacturing and plastic product Designer should be aware of its need at the outset of the design process. This allows considerations for design requirement to be taken into account.
Nominal values for Draft angle :
- 3 Degrees is the nominal Draft angle.
- 7 Degrees for textured surface.
- At the minimum of 0.5 Degrees can be manufactured by special tools. But it will increase the manufacturing cost.
Tooling Axis Creation :
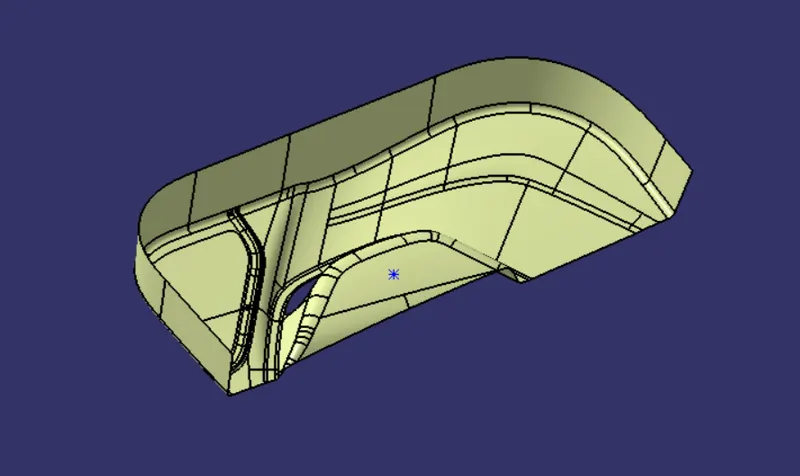
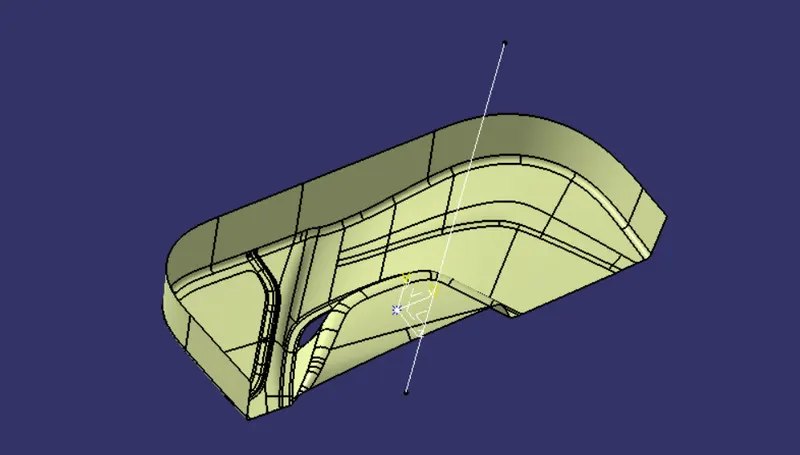
First step is to observe the given class-A surface deeply and we can say the larger flat area which is perpendicular to the Tooling axis. so by considering this things for this class-A surface tooling direction will be in Y-direction. So we create the point on the flat surface as shown in figure.
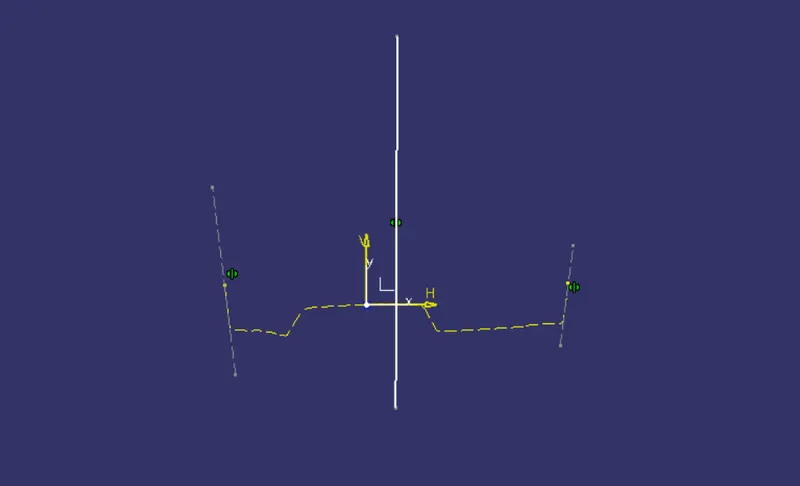
And next step is to create the reference axis in the X-direction using sketch and bisect line as shown in figure.
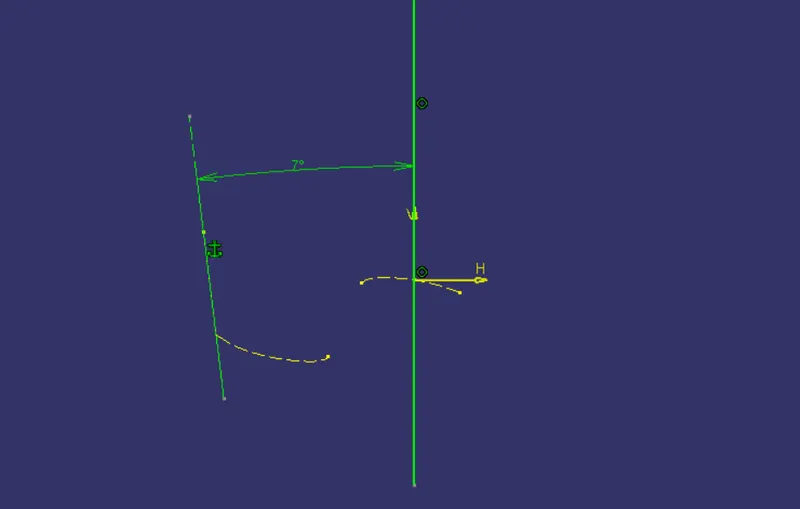
Next step is to create the reference axis in the Z-direction using sketch and bisect line as shown in figure.
Now create the surfaces using the both reference line we got as shown in figure.
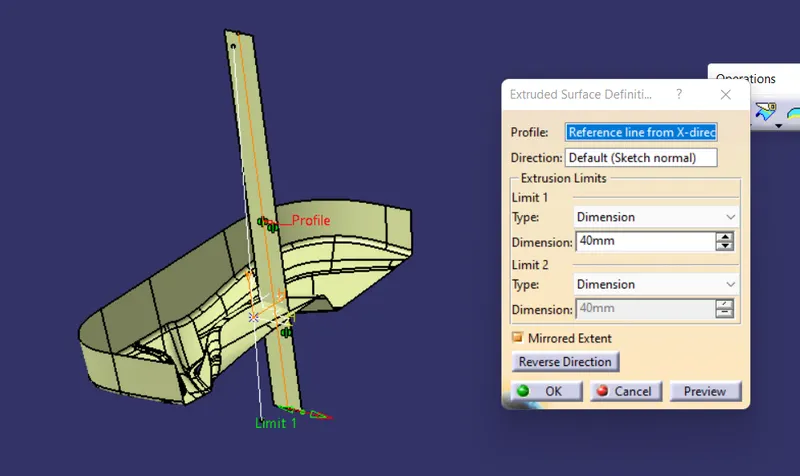
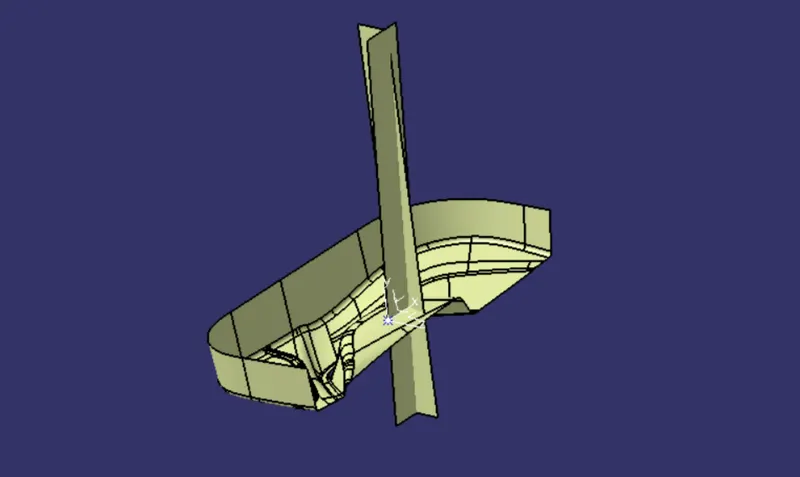
Now from the two surface intersection line will be the main tooling axis so using intersection we get that tooling axis as shown in figure.
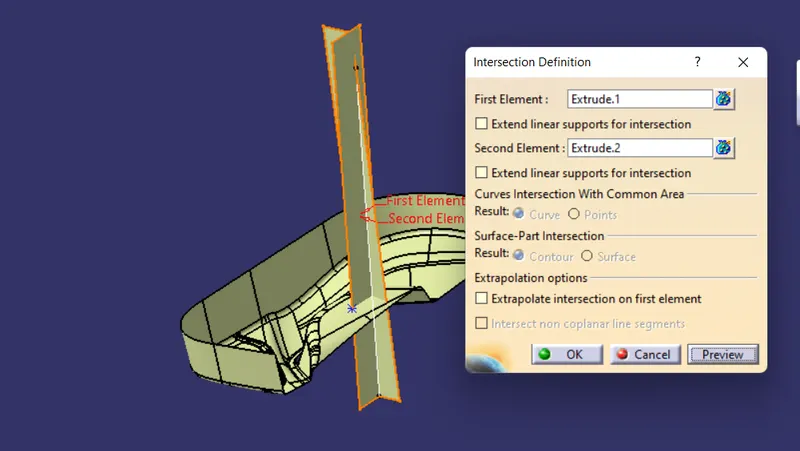
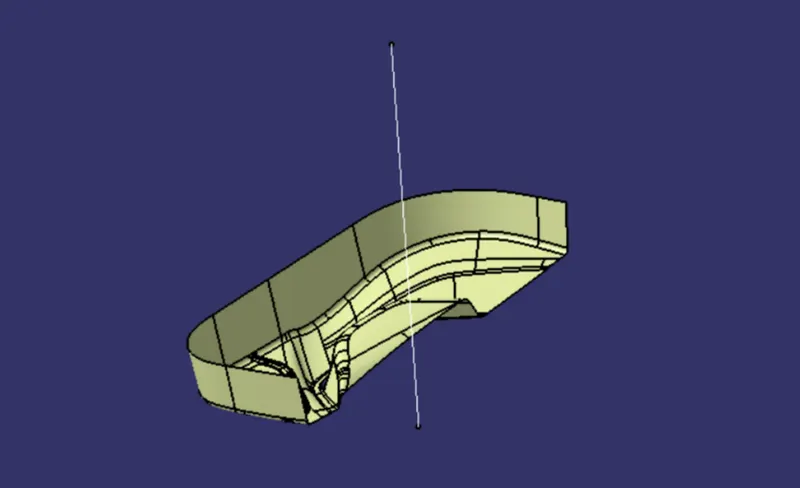
And hide the other reference axis line as shown in figure.
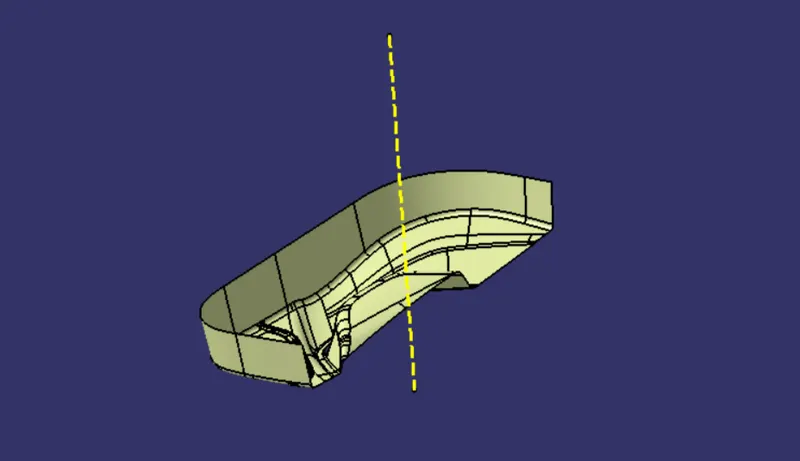
And now to view clearly change the line type and line color using properties as shown in figure.
Draft Analysis :
- The part created has to be changed to material mode in display frame.
- Compass is enabled and align it along with the tooling direction.
- Lock command is then applied to fix compass along with tooling axis.
- Color codes are classified and Draft angle is applied.
- Running point analysis is used to display permissible draft angle.
Draft analysis for Class-A surface :
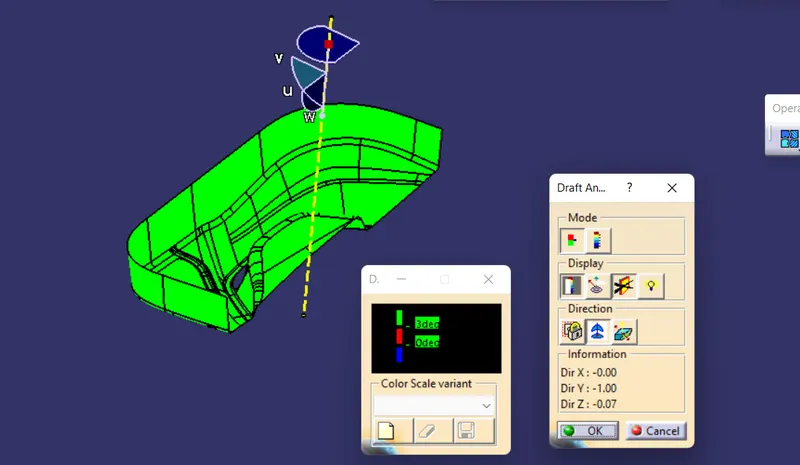
Given Class-A surface :
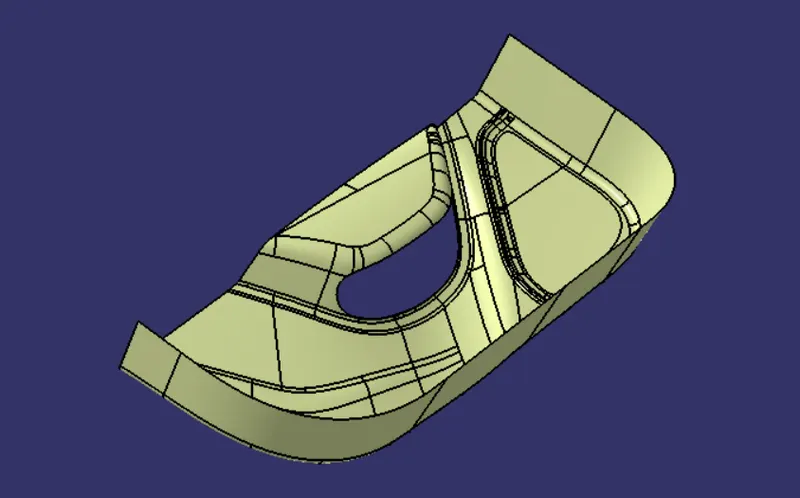
Created Class-B surface :
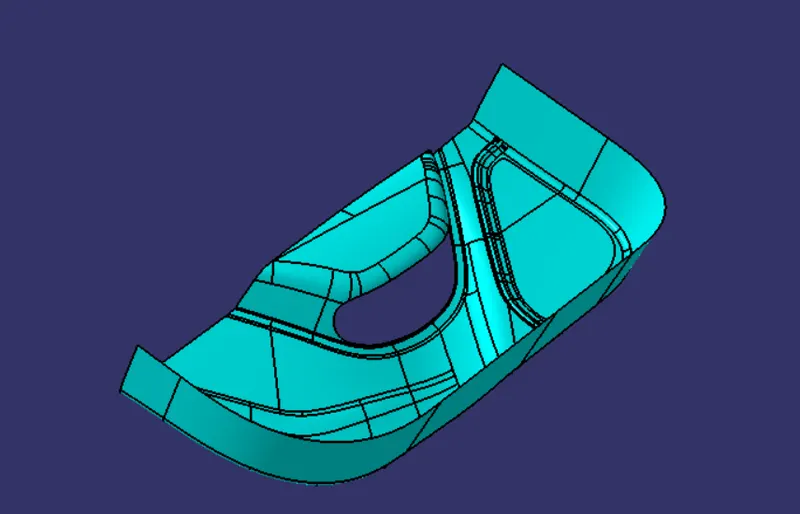
Created Class-C surface :
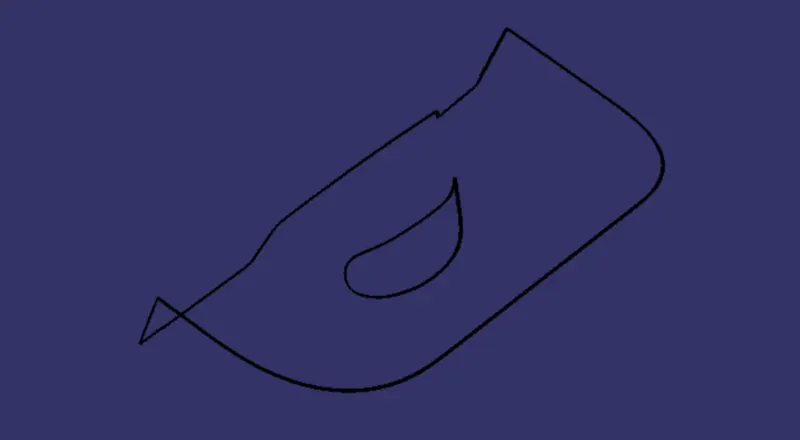
Closed surfaces :
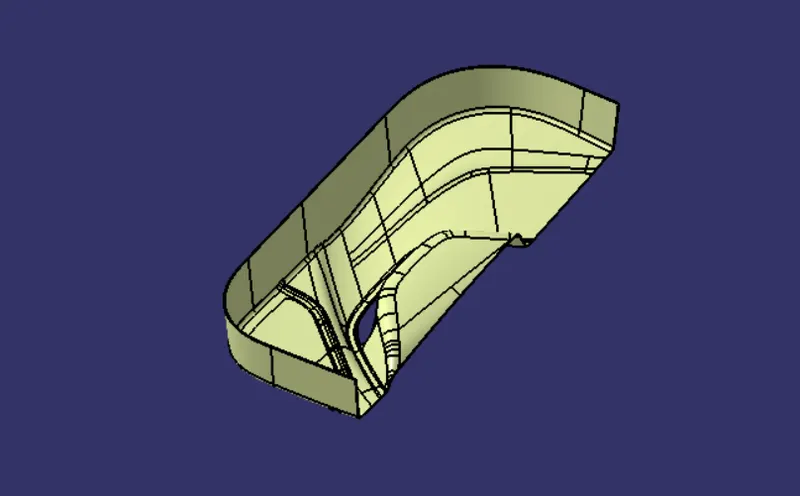
Solid part : Created by using the close surface tool.
3-2-1 Location Principle :
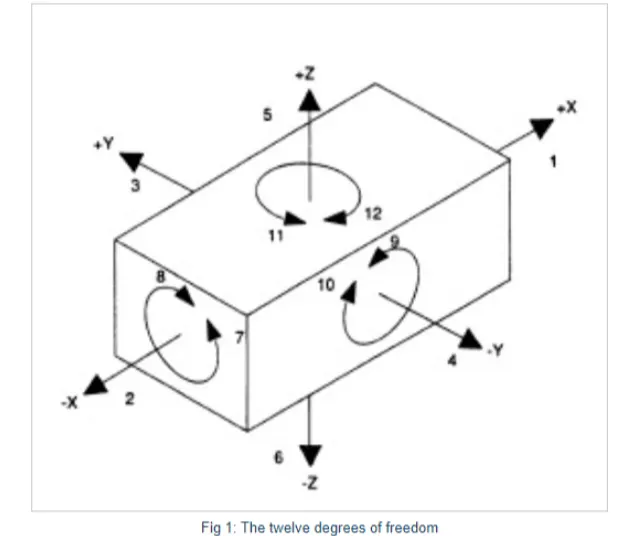
Any 3 dimensional object in space has 12 degrees of freedom along the 3 axes
- Translational position along the X-axis
- Translational position along the Y-axis
- Translational position along the Z-axis
- Rotational position along the X-axis
- Rotational position along the Y-axis
- Rotational position along the Z-axis
3-2-1 principle entails three steps that employ three, then two, then one fixed point of known location. Since that adds up to six fixed points, its also known as the six point method.
In the three steps of the 3-2-1 method, three mutually perpendicular planes, called datum planes, are introduced, one at each step. These three planes define the workpiece position, and together with opposing clamping forces fully contrain the part.
First plane :
Geometry tells us that three points are required to define a plane. This is the "3" in 3-2-1. so three specific points are used to define the first plane. The part's six degrees of freedom have now been reduced to three. It can still move along the X axis, and it can still be rotated about the Z axis. (The part cannot move along the Z axis because it is held against the plane by clamping force).
Second plane :
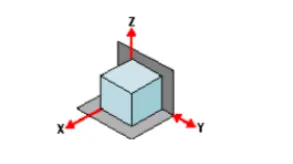
A second plane, if it is perpendicular to the first, can be defined by two points, the "2" in 3-2-1. The part is now constrained to one degree of freedom movement along the Y axis.(The part cannot move along the X or Z axis because it is held against the planes by clamping forces)
Third Plane :
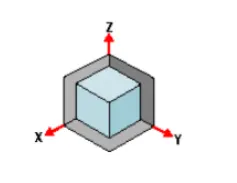
A third plane if it is perpendicular to both of the first two planes, can be defined by one point, the "1" in 3-2-1. The part is now entirely constrained. It cannot move along or rotate about the X, Y or Z axis. (Remember that the part is held against each of the three planes by clamping forces.)
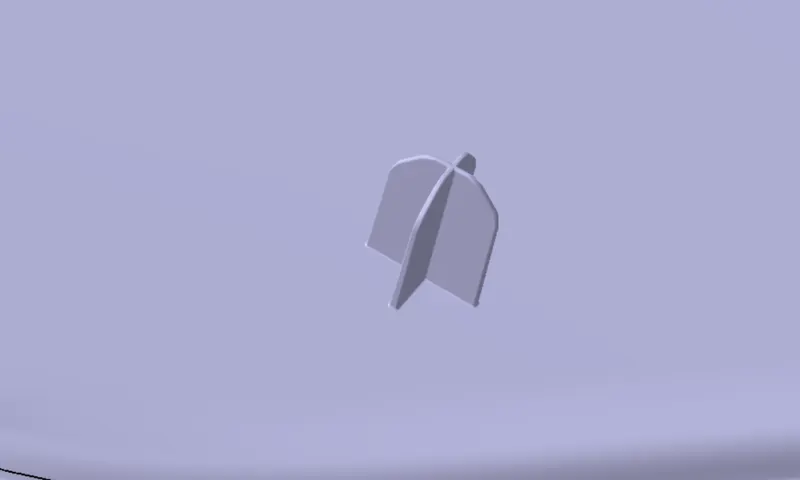
4 way and 2 way locators :
4 way locators restricts 4 degrees of freedom along 2 axis and 2 way locators restricts 2 degrees of freedom along 1 axis.
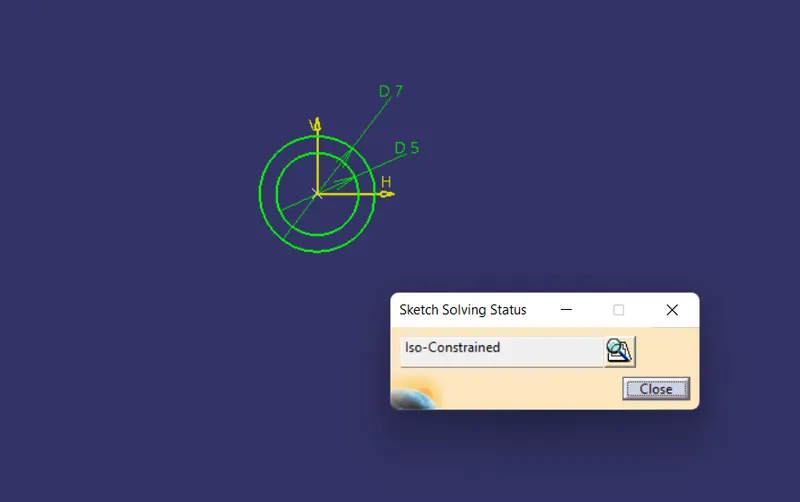
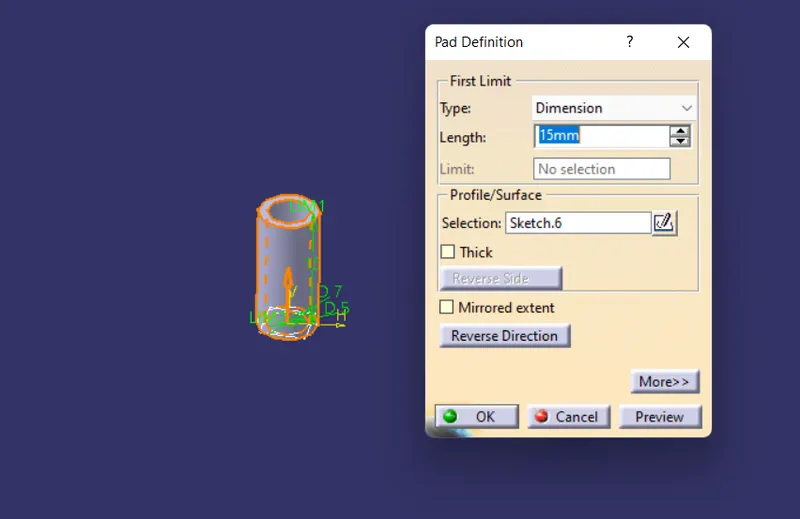
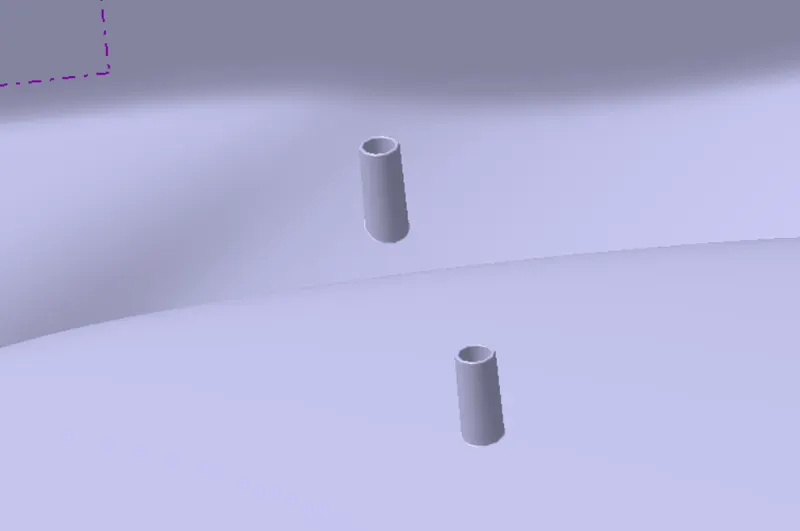
Heat Staking :
Heat staking technology is quite simple in concept. Whenever two or more components need to be attached to one another, and at least one is made of a thermoplastic, a combination of heat and pressure can be used to reform the plastic to the many shapes or profiles to retain or join the parts together.
This creates a solid, hardware-free bond that uses the plastic's inherent strength to keep the finished assembly together.
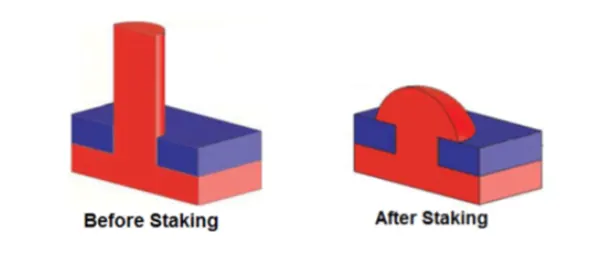
The main advantage to heat staking when compared to fastener to fastener-based technologies, is that manufacturers can perform all heat staking in one machine cycle and motion versus individual motions required for each fastener. A secondary benefit is that the manufacturers do not need to change the base material. It can remain "AS-IS" while the plastic is heat staked to conform to its final dimensions.
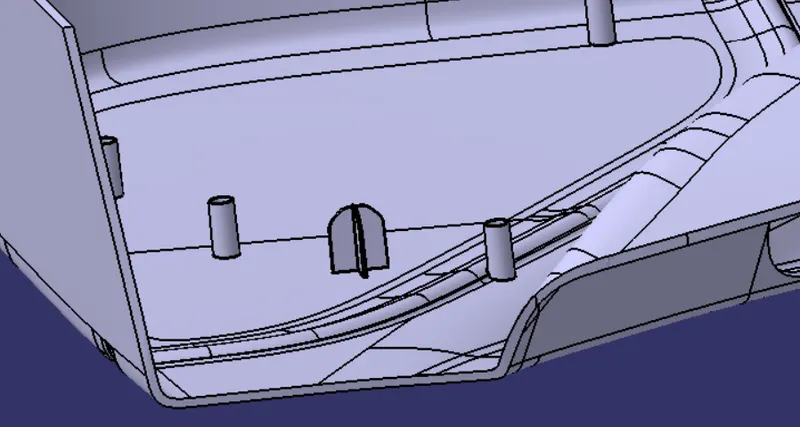
Locators Creation :
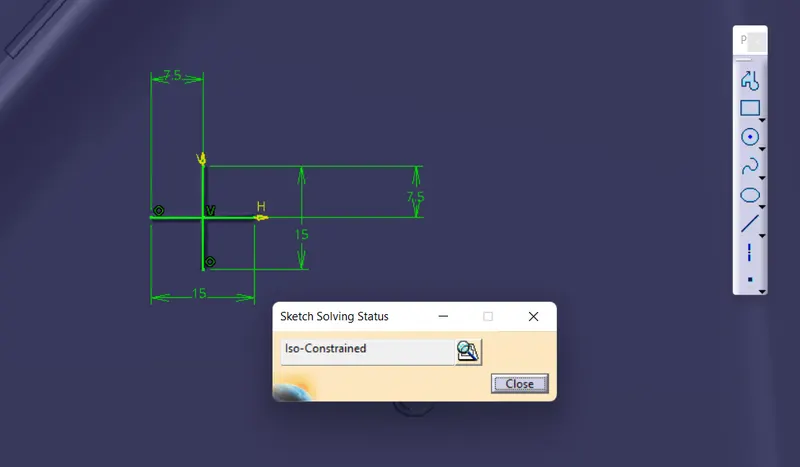
Sketch for locator :
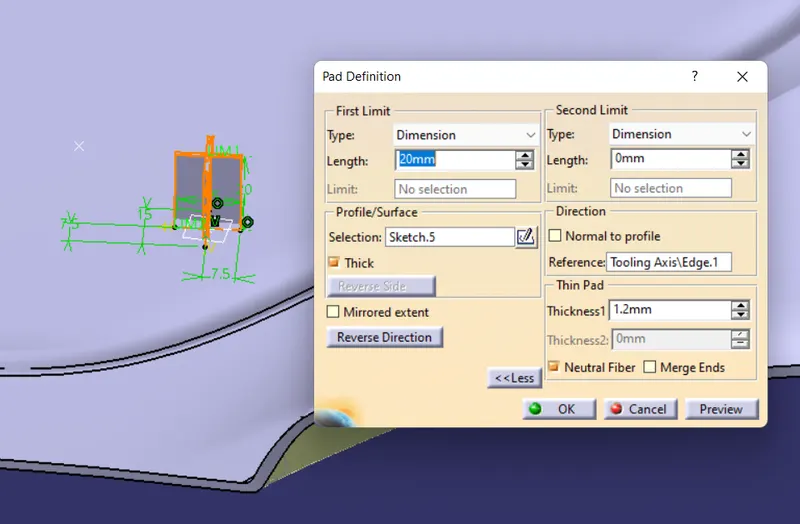
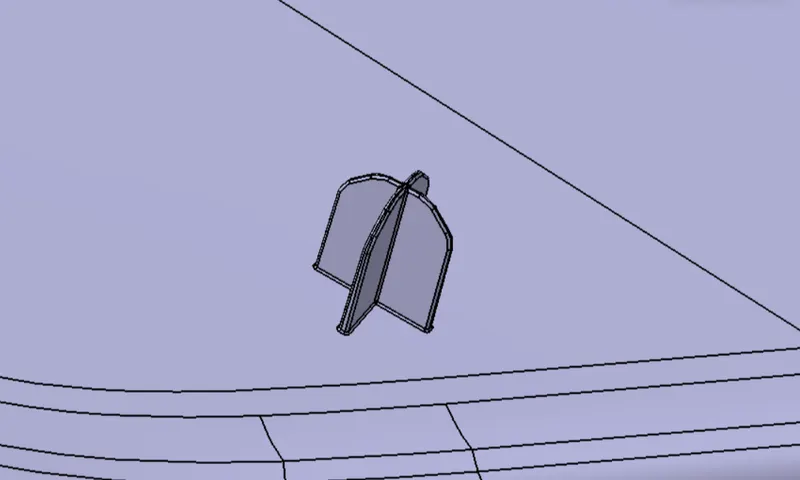
Heat stake creation :
Sketch for Heat stake :
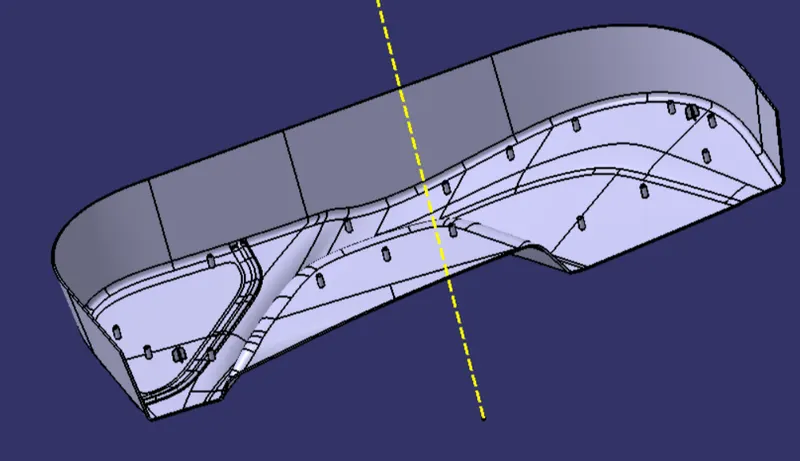
Final component :
Closer view :
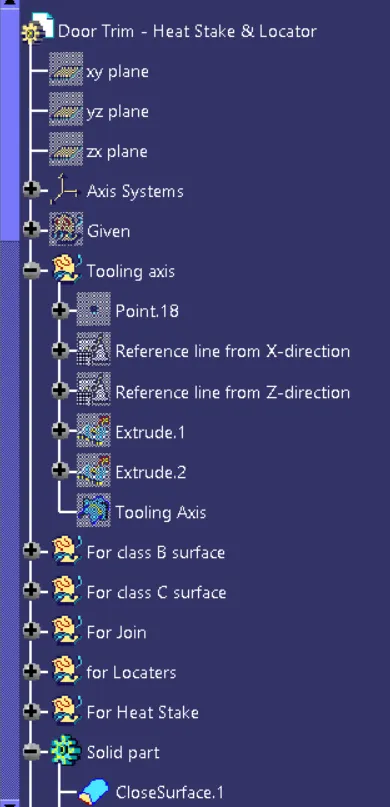
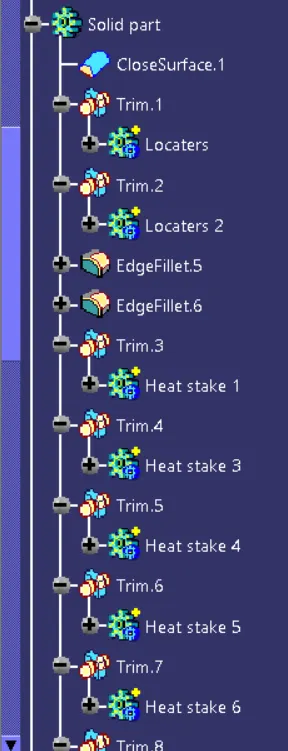
Tree Structure :
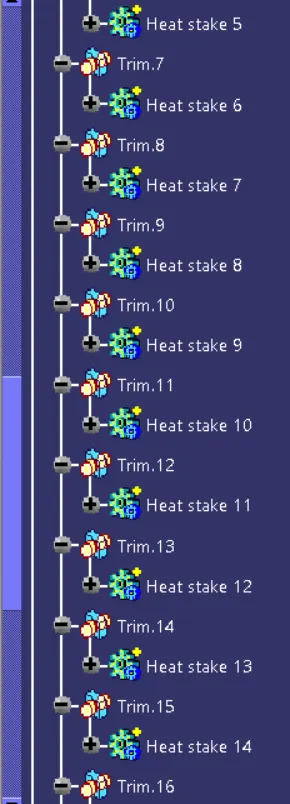
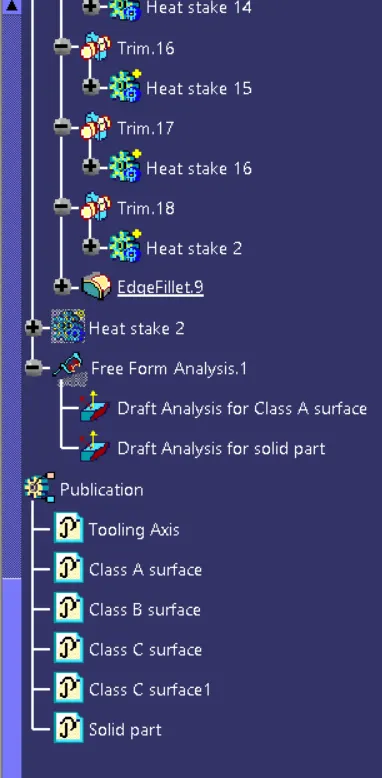
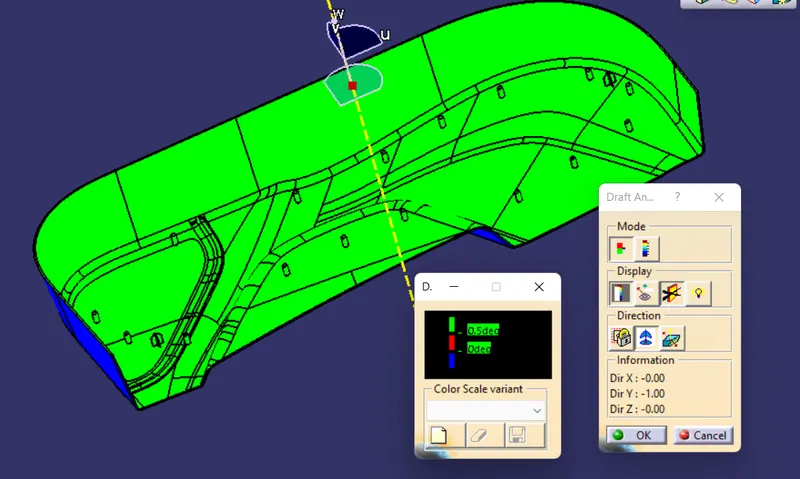
Draft Analysis :
- The part created has to be changed to material mode in display frame.
- Compass is enabled and align it along with the tooling direction.
- Lock command is then applied to fix compass along with tooling axis.
- Color codes are classified and Draft angle is applied.
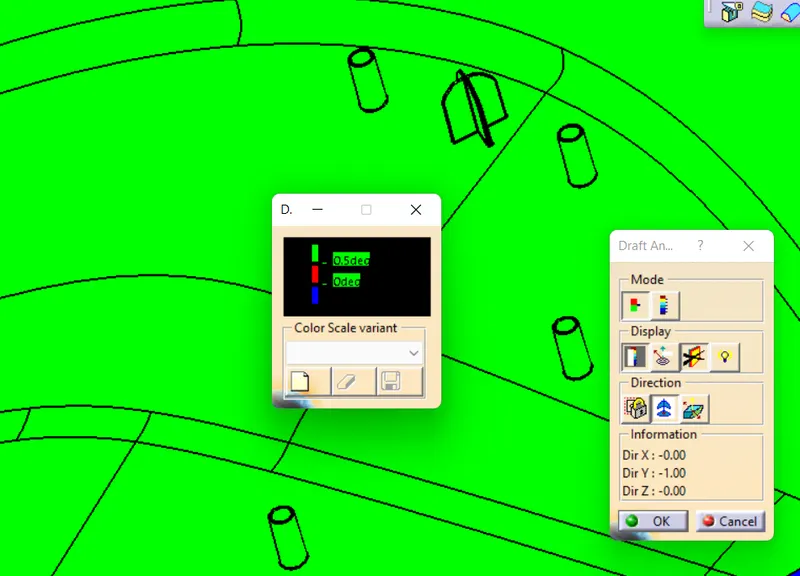
- Running point analysis is used to display permissible draft angle.
Draft analysis - Final component :
Closer view :
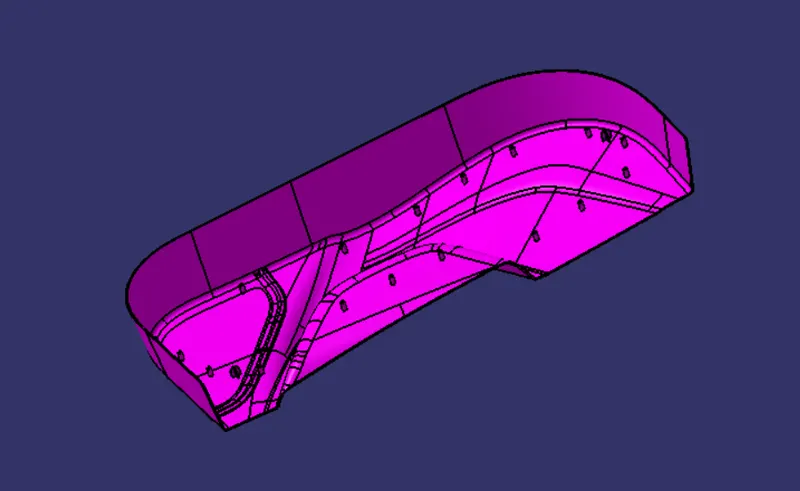
Iso-metric view :
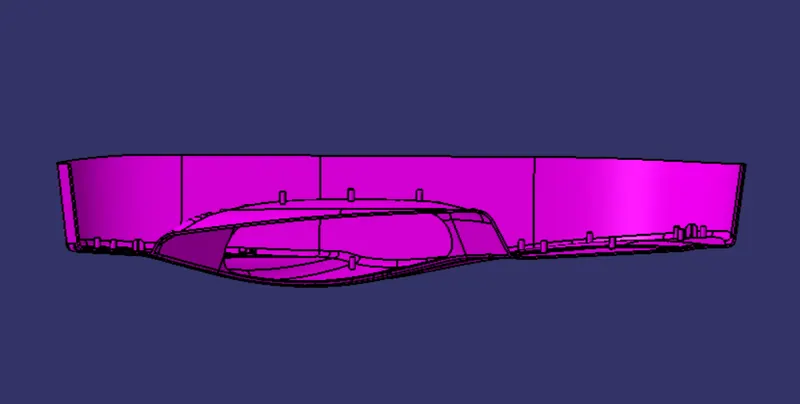
Front view :
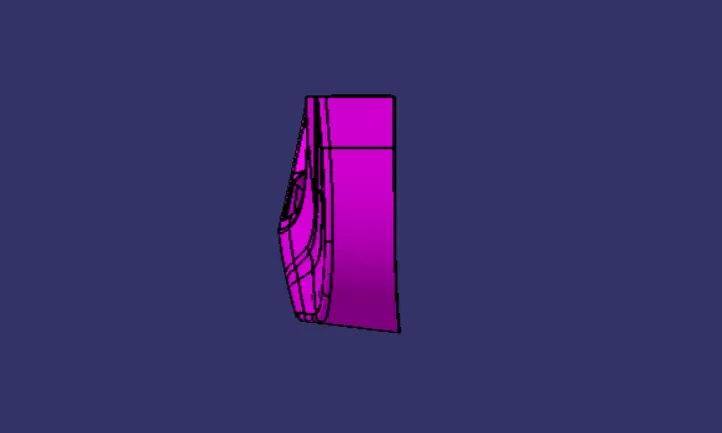
Side view :
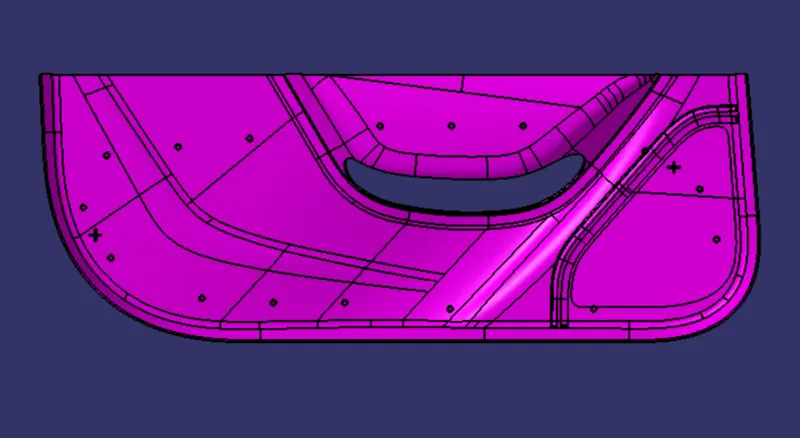
Top view :
Conclusion :
Hence the Door trim lower plastic component through the given Class-A surface and attach the engineering features such as Locaters and Heat stakes are create successfully and the Draft analysis for the final component also performed successfully.