Week 9 - Project 1 - Door Trim Lower with Engineering Features
Object:- Design of Door Trim Lower with Engineering Features
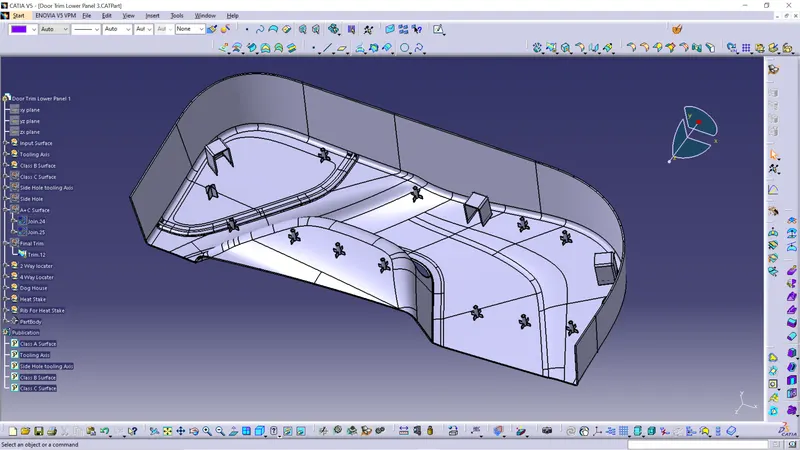
Engineering Features:-
Heat Stake:-
Heat staking also known as thermoplastic staking is the process of joining two dissimilar materials together. In heat staking we use local heating and cooling to raise the temperature of plastic components and allow plastic reforming to be carried out. This reforming can be used in a wide variety of applications.
Applications range from staking plastic bosses for assembly of car door panels to joining PCB’s to plastic housings. Benefits of this technique include; no vibration damage, no particulates, the ability to stake metalized coated applications and the capability to stake in difficult to access or restricted areas.
Advantages of Heat Staking
- Consistent, Fast & Economical Alternative to Rivets & Screws.
- Joins different materials Eg: Plastic to plastic , plastic to non-plastic or join 2 non-plastics.
- Able to handle difficult to weld plastics.
- Simple mechanism and accurate control.
Industry Applications
- Automotive : Reliable solution for interior parts, welding bumpers, tail light assemblies, dashboards & many more parts
- Textile : Creates durable seals without the need for glues, clips and yarns in product designs
- Appliances : Component welding for large or small household appliances
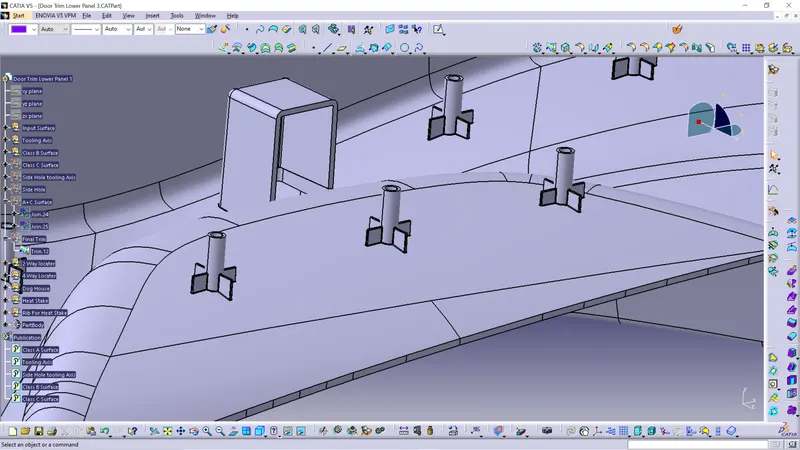
Heat Stakes in car door panel:-
Locators:-
Locators provide a positive stop for the workpiece. Placed against the stop, the workpiece cannot move. Clamps, on the other hand, rely only upon friction between the clamp and the clamped surface to hold the workpiece. Sufficient force could move the workpiece.
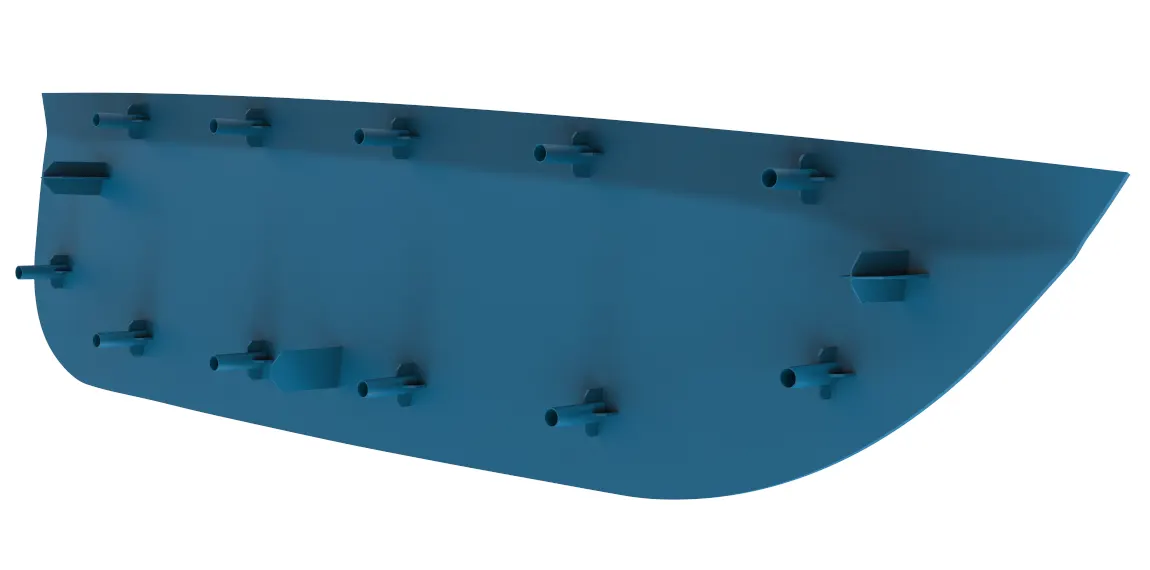
types of locators
4 way locator:-
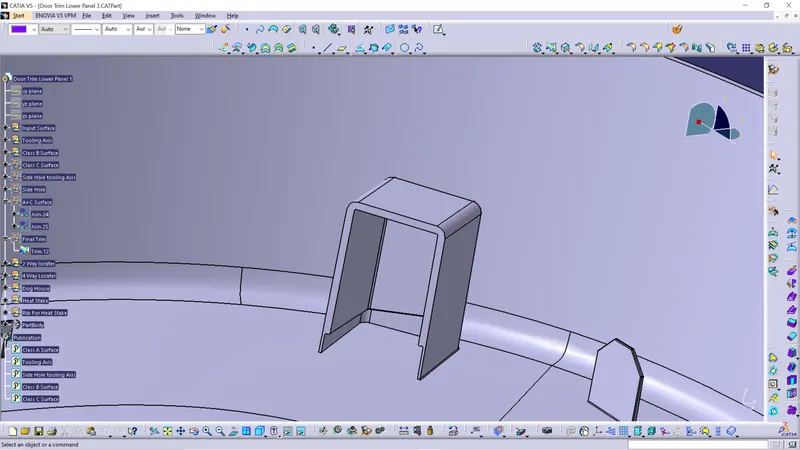
A round locating pin located concentrically in a hole is a common application of a 4-way pin, and helps to further secure the piece. 4-WAY LOCATORS: 4-way mean you prevent movement at 2 axes (+X, -X, +Y and -Y) on the plane. Generally, you have cylindrical pin on the fixture and circular hole at workpiece part.
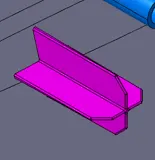
1.WALL THICKNESS:
Thick sections waste material and are simply uneconomic. So solid shapes that would do the job well in wood or metal must be transformed to a 'shell' form in plastics. This is done by hollowing out or 'coring' thick parts so you are left with a component which regardless of complexity is composed essentially of relatively thin walls joined by curves, angles, corners, ribs, steps and offsets. As far as possible, all these walls should be the same thickness. Wall thickness guide range is 0.75 mm to 3 mm for reinforced materials 0.5 mm to 5 mm for unreinforced materials.
Wall thickness = As material thisckness
Coaring wall Thickness = Guide range is 40% of material thisckness
2.DRAFT ANGLE:Tooling must be cleared for easy ejection of the component, from the core cavity. In order to clear tooling certain value of draft is given to the component. Minimum of 2-3deg is provides on all plastic components.
Minimum draft angle for the for all engineering features is 0.5 Degree (According to Skill-Lync data)NOTE:- These data are provided by Skill-Lync
Draft Analysis:-
The draft analysis technique is used to analyze whether our part model created in CAD is manufacturable based on the draft condition applied. Here the part should get easily removed from the panel dies (in case of Sheet metal part) or Mold (in case of plastic).
No parts can be ejected from the tool if it is having a straight 90-degree profile from its base surface. A small draft angle is provided to each and every area of the component in order to get easy removal of the component from the tool.
Here we are providing a direction in which components should eject in order to get easy removal of components from the tool. In other words, it also lets us know whether the model is having a draft angle and how much is the draft angle from the tool direction.
Minimum draft angle for the for all engineering features is 0.5 Degree (According to Skill-Lync data)