Week 8 - Simulating Cyclone separator with Discrete Phase Modelling
- Abstract:
A CFD analysis of a cyclone separator is performed. The separation efficiency is found. Firstly the diameter of the particles is varied. Then the velocity at the inlet is varied with particles of constant diameter. The Physics of the problem is set up in Ansys Fluent. The Post-processing of the results obtained is done is CFD-Post.
- Objective:
- To perform an analysis on a given cyclone separator model by varying the particle diameter from 1 μm to and calculate the separation efficiency in each case. Discuss the results. [Use both the velocity's as 3m/sec.]
- To perform an analysis on a given cyclone separator model by varying the particle velocity from 1 m/sec to 5 m/sec and calculating the separation efficiency and pressure drop in each case. Discuss the results. [Use particle diameter size as 5 μm for all cases & keep flow velocity same as particle velocity]
- Cyclone Separator:
Cyclone separators are separation devices that use the principle of inertia to remove particulate matter from flue gases. Cyclone separator is one of many air pollution control devices known as pre-cleaners since they generally remove larger pieces of particulate matter. This prevents finer filtration methods from having to deal with large, more abrasive particles later on. In addition, several cyclone separators can operate in parallel, and this system is known as a multi-cyclone.
It is important to note that cyclones can vary drastically in their size. The size of the cyclone depends largely on how much flue gas must be filtered, thus larger operations tend to need larger cyclones. For example, several different models of one cyclone type can exist, and the sizes can range from a relatively small 1.2-1.5 meters tall (about 4-5 feet) to around 9 meters (30 feet)—which is about as tall as a three-story building.
Working:
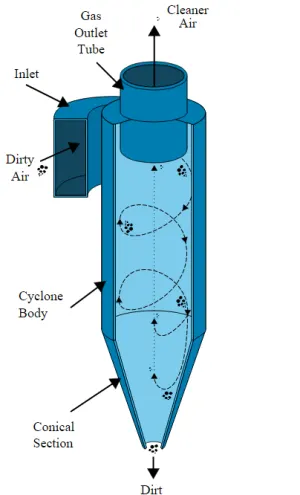
Cyclone separators work much like a centrifuge, but with a continuous feed of dirty air. In a cyclone separator, dirty flue gas is fed into a chamber. The inside of the chamber creates a spiral vortex, similar to a tornado. This spiral formation and the separation is shown in the Figure below. The lighter components of this gas have less inertia, so it is easier for them to be influenced by the vortex and travel up it. Contrarily, larger components of particulate matter have more inertia and are not as easily influenced by the vortex.
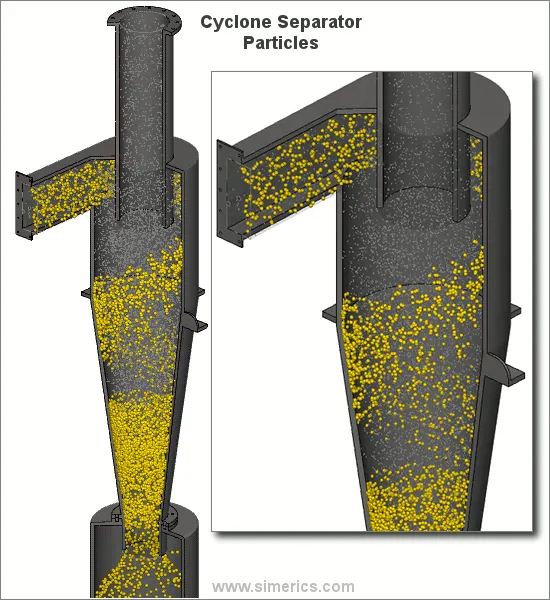
Most cyclones are built to control and remove particulate matter that is larger than 10 micrometers in diameter. However, there do exist high-efficiency cyclones that are designed to be effective on particles as small as 2.5 micrometers. As well, these separators are not effective on extremely large particulate matter. For particulates around 200 micrometers in size, gravity-settling chambers or momentum separators are a better option.
Out of all of the particulate-control devices, cyclone separators are among the least expensive. They are often used as a pre-treatment before the flue gas enters more effective pollution control devices. Therefore, cyclone separators can be seen as "rough separators" before the flue gas reaches the fine filtration stages.
Effectiveness:
Cyclone separators are generally able to remove somewhere between 50-99% of all particulate matter in the flue gas. How well the cyclone separators are actually able to remove this matter depends largely on particle size. If there is a large amount of lighter particulate matter, fewer of these particles are able to be separated out. Because of this, cyclone separators work best on flue gases that contain large amounts of big particulate matter.
There are several advantages and disadvantages of using cyclone separators. First, cyclone separators are beneficial because they are not expensive to install or maintain, and they have no moving parts. This keeps maintenance and operating costs low. Second, the removed particulate matter is collected when dry, which makes it easier to dispose of. Finally, these units take up very little space. Although effective, there are also disadvantages in using cyclone separators. Mainly because the standard models are not able to collect particulate matter that is smaller than 10 micrometers effectively and the machines are unable to handle sticky or tacky materials well
Description of the project statement:
1. With varying the particle diameter, at a constant velocity at the inlet the flow is simulated. separation efficiency is found.
2. With varying the velocity at the inlet, at a constant diameter of the particles, the flow is simulated. separation efficiency and pressure drop in the cases is found.
Changing particle diameter from 1 micrometer to 5 micrometers, with velocity as 3 m/s:
1. Geometry setup:
a. Choose the Fluid flow (fluent) module and start with editing geometry.
b. Import the step file of the model into Spaceclaim.
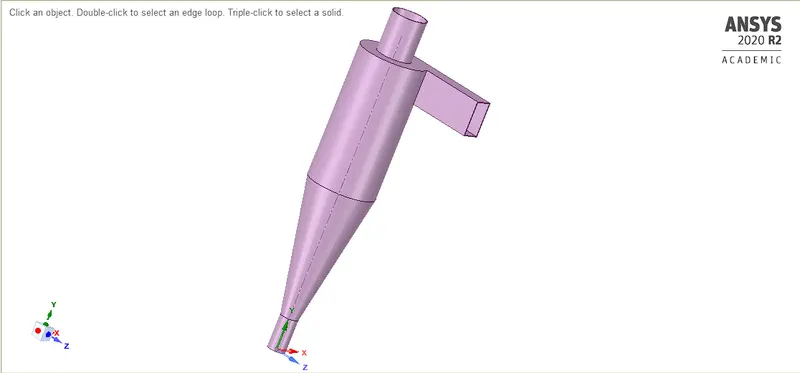
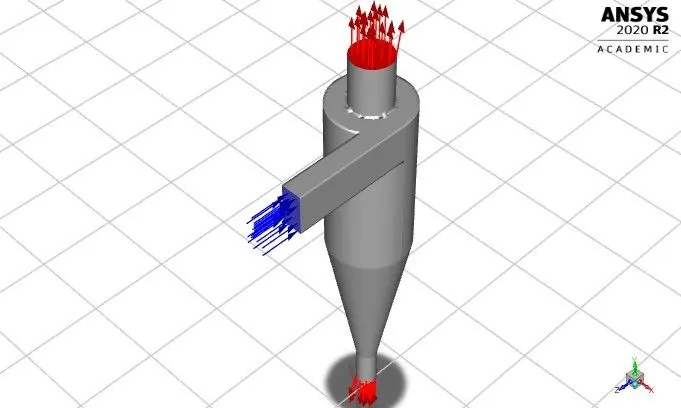
c. Fluid volume is extracted from the geometry by using the prepare option. so that we can analyze the fluid flow of the cyclone separator.
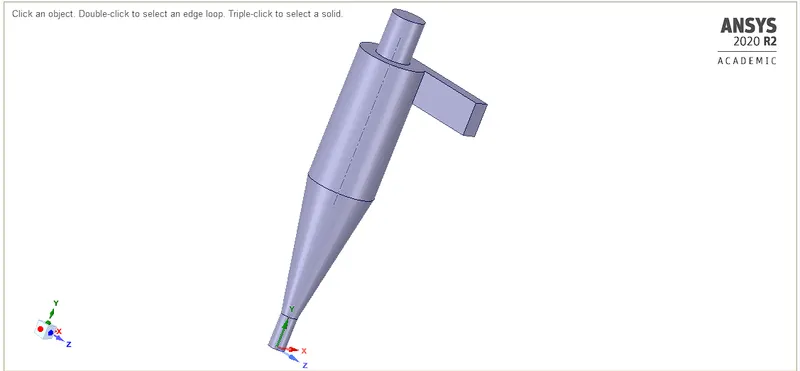
d. Hide the previous geometry and suppress physics since we are only interested in the fluid flow and not the external surface.
2. Mesh setup:
Mesh stats:
1. Main element size: 9mm
2. Method = Cartesian method
3. Cartesian element size= 5.2623mm
4. No. of elements= 140228
Mesh quality:
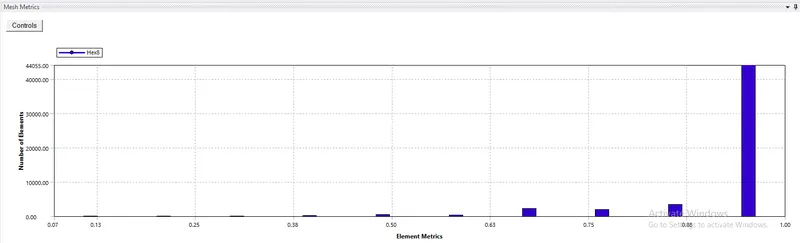
a. After up-streaming the model to meshing, choose generate mesh to generate the base mesh but since the number of particles entering the inlet depends on the refinement of the mesh, it's better to refine the mesh appropriately.
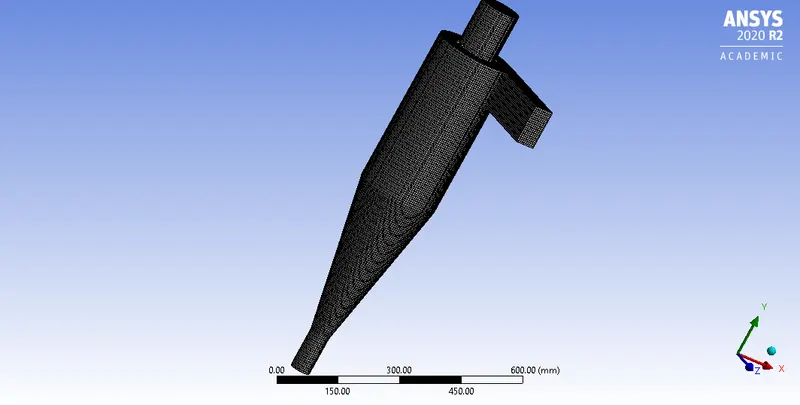
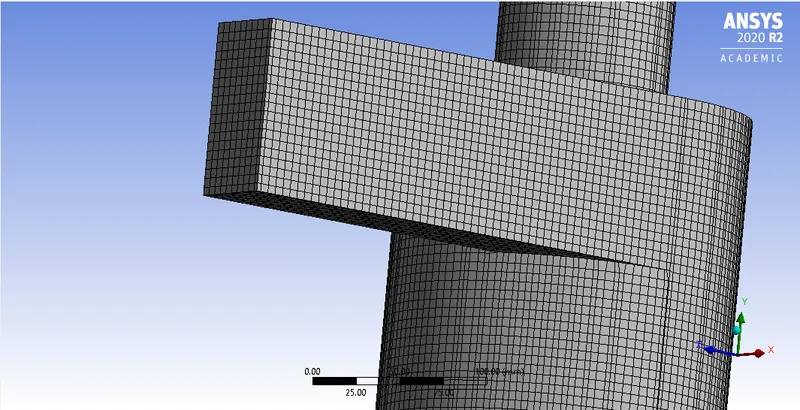
b. Providing named selection:
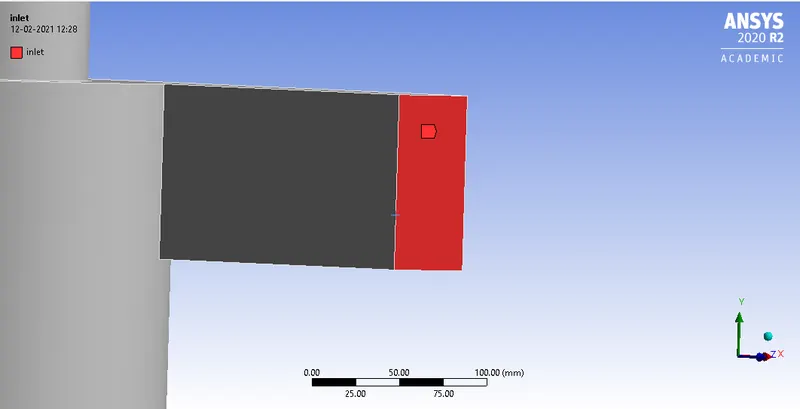
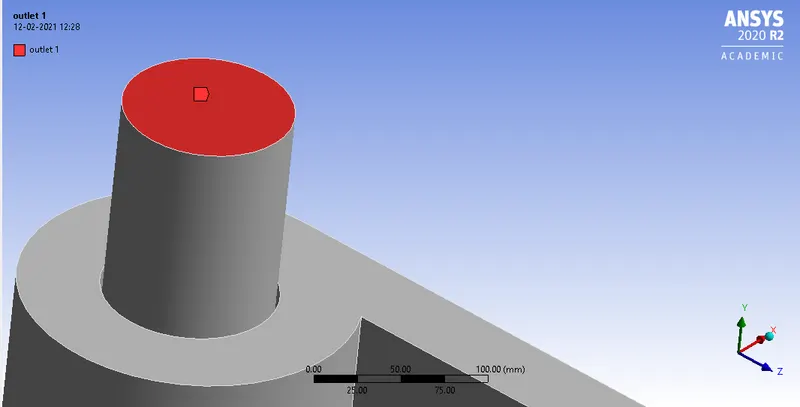
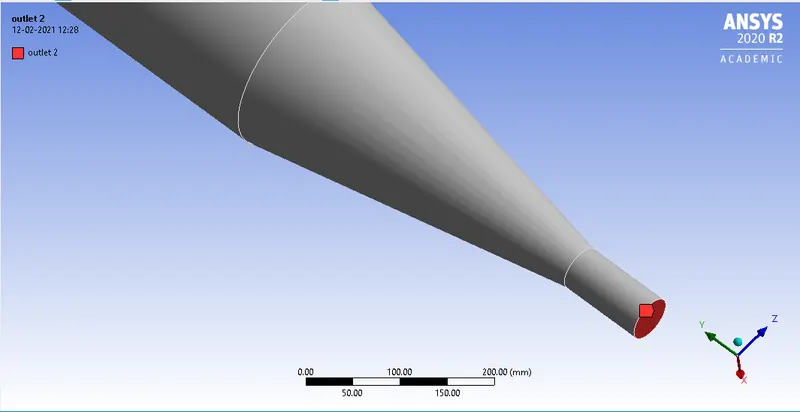
The face-selecting tool is selected. The inlets, outlet (top), and outlet(bottom) is named. The inlet is through which the particles enter the lighter impurities escape through the top, and the heavier impurities are trapped in the bottom.
- Solving:
Physics setup:
1) General conditions:
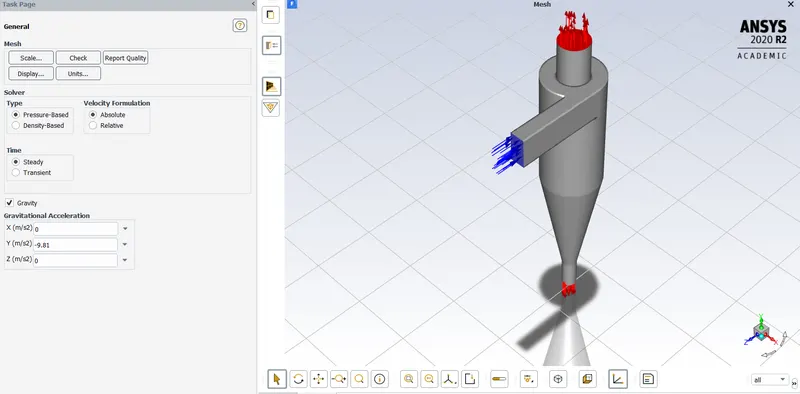
This analysis involves the orientation of the cyclone separator. As it is in the x-y plane, the acceleration due to gravity needs to be turned on. As acceleration due to gravity acts upwards, the g value is assigned as -9.81 in the positive y-axis.
Pressure based solver is used. The steady-state analysis is done and the velocity formulation is normal to the boundary and absolute.
2) Physics setup:
- Turbulence modeling:
The K-epsilon(2 equation) model with RNG and swirl-dominated flow is selected. The wall mofunctions are standard wall functions.
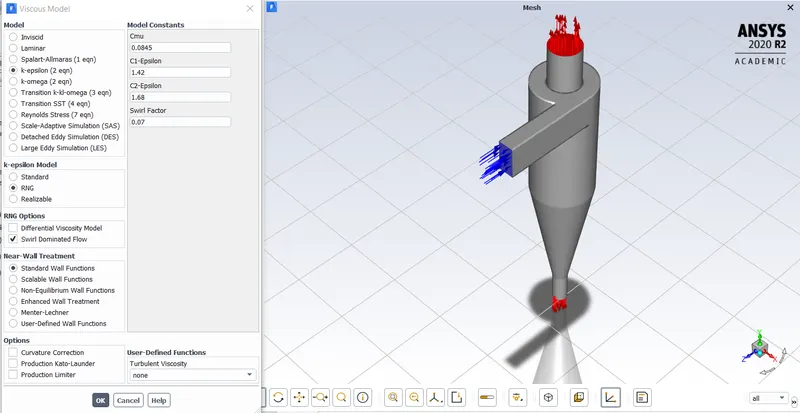
Since temperature is not involved, the Energy is not turned on.
- DPM:
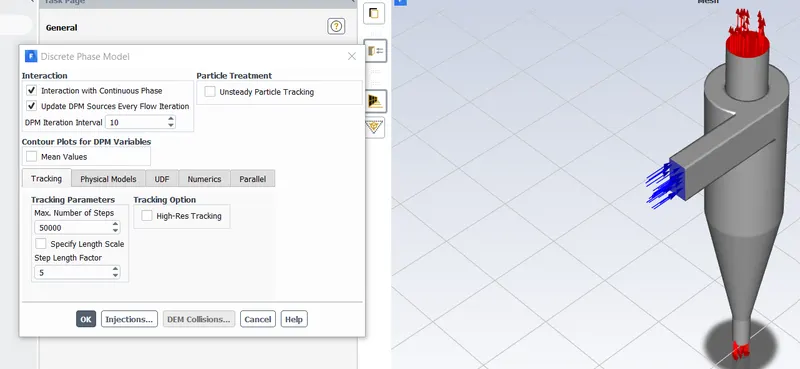
Discrete phase modeling is opted for.
The model is enabled for interaction with the continuous phase. The DPM interval level is 10.
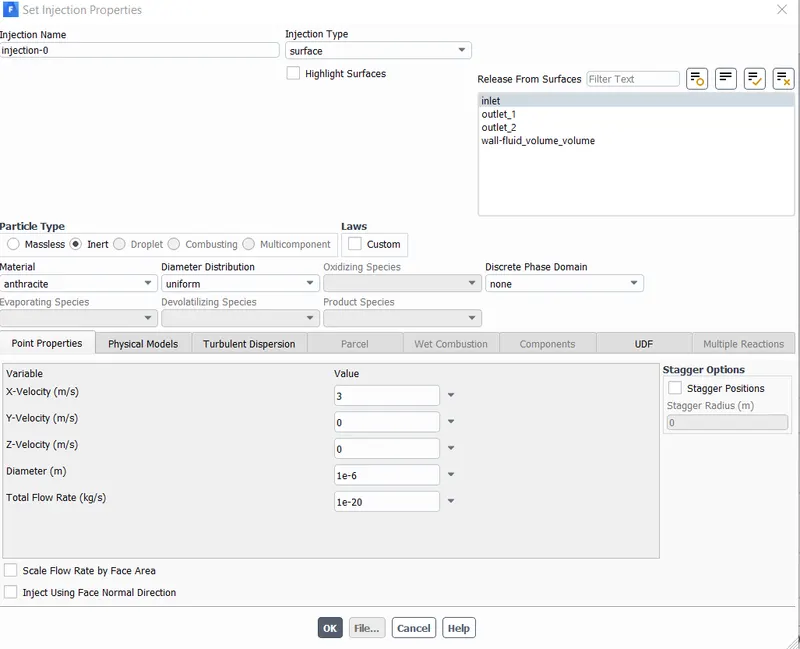
For injection, the particle type is inert. From the fluent database, anthracite is selected. It is released from the inlet, with velocity in the x-direction being 3m/s. This velocity may be manipulated further. The particle diameter chosen for the first analysis is one micrometer. The particle diameter is varied from one micrometer to five micrometers to calculate the separation efficiencies.
- Boundary conditions:
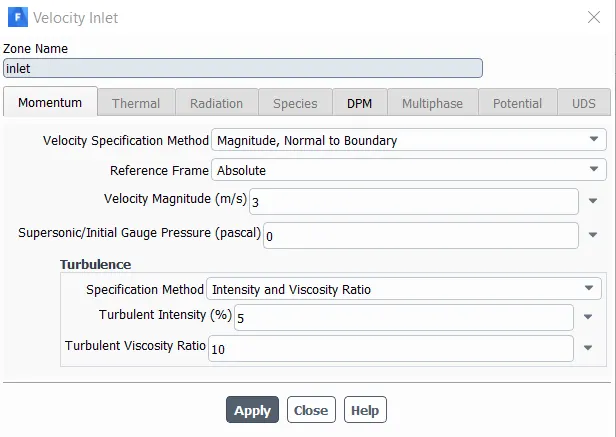
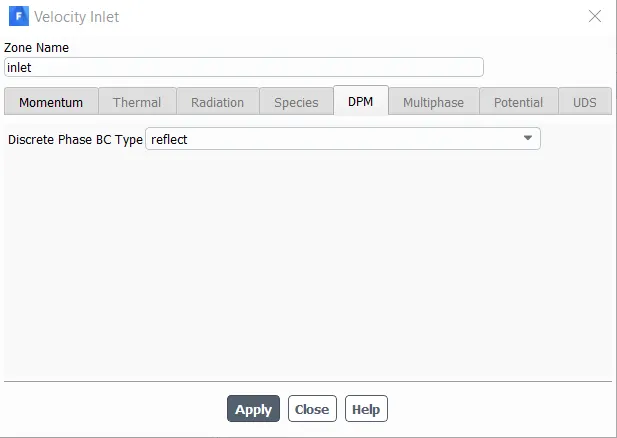
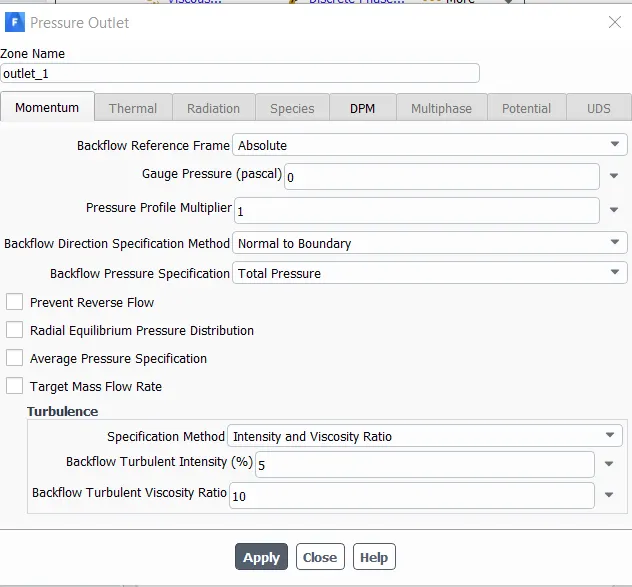
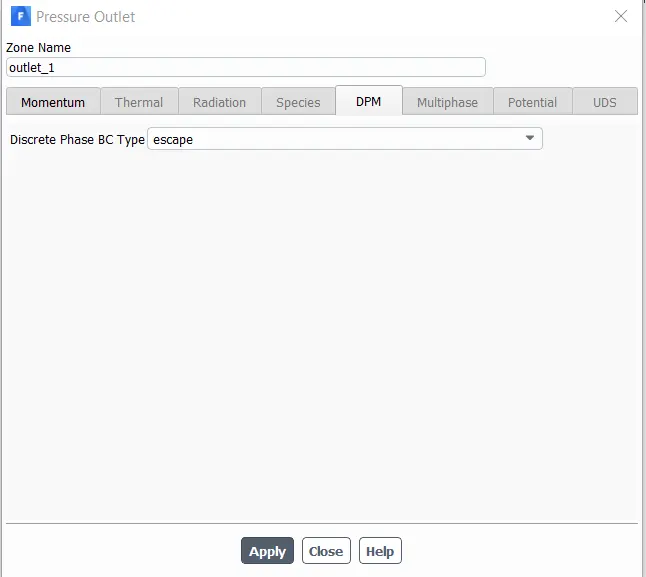
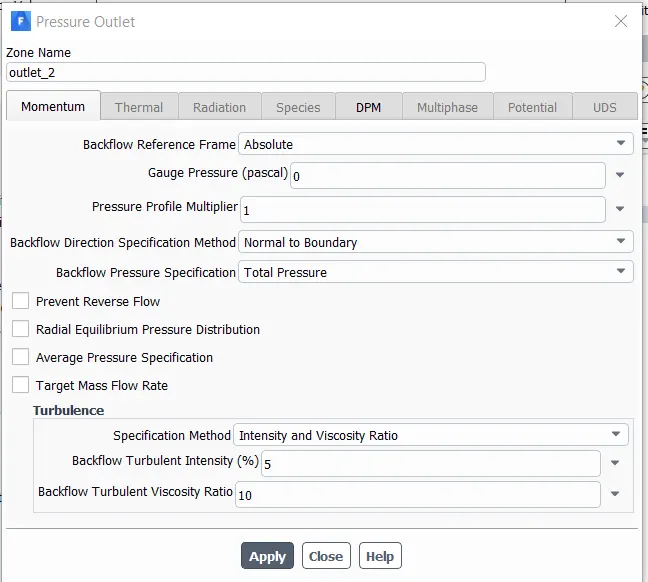
The boundary conditions are provided to three named selections, inlet, outlet(1)top, and outlet(2) bottom.
For the inlet, the momentum conditions are v3locity is 3m/s in the x direction, being absolute and normal to the boundary. The DPM condition is reflected. This signifies that the particles are not allowed to escape or get trapped in the inlet.
For the top outlet, the Momentum condition is basically a pressure condition, The DPM condition is escaping. Particles can escape from this Boundary
The bottom outlet is also a pressure outlet, with the DPM condition being trapped.
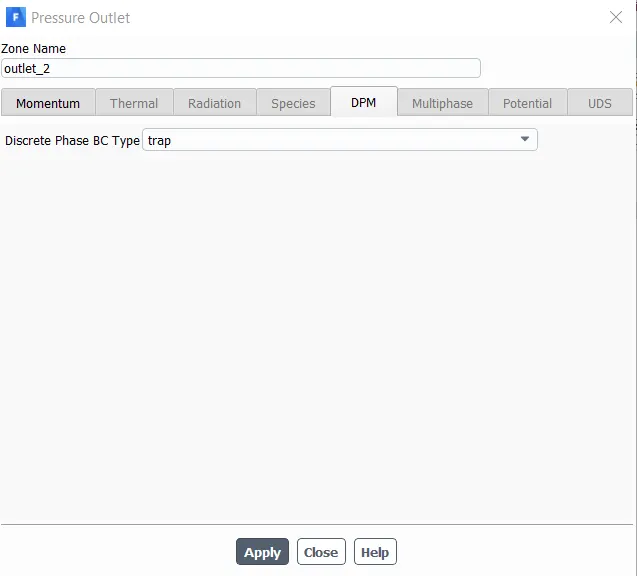
- Solution methods:
The pressure velocity coupling is chosen as COUPLED scheme. The gradient is least square cells based. Pressure, Momentum, Turbulent kinetic energy, and turbulent dissipation rate are second-order upwind.
- Initialization:
Standard initialization is done with flow from inlets.
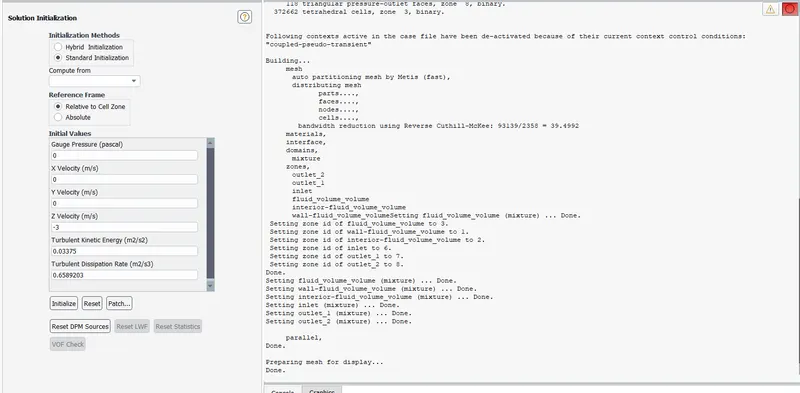
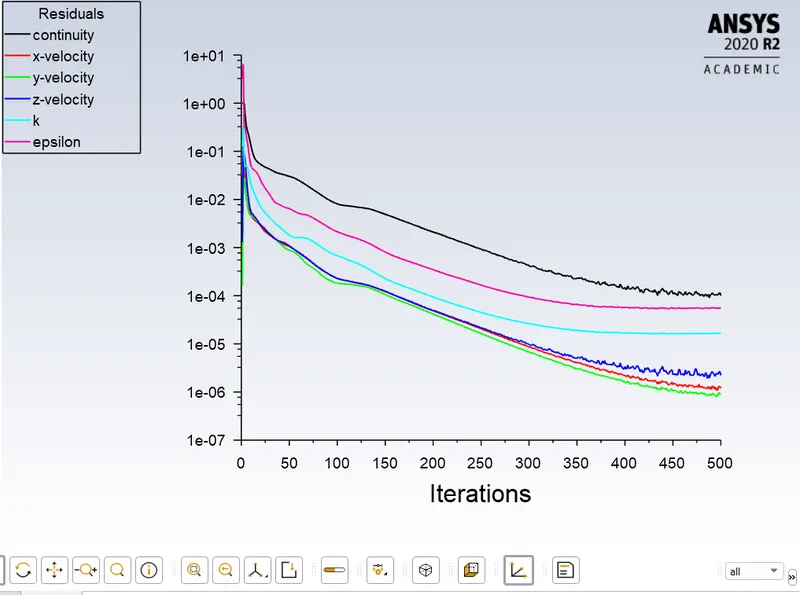
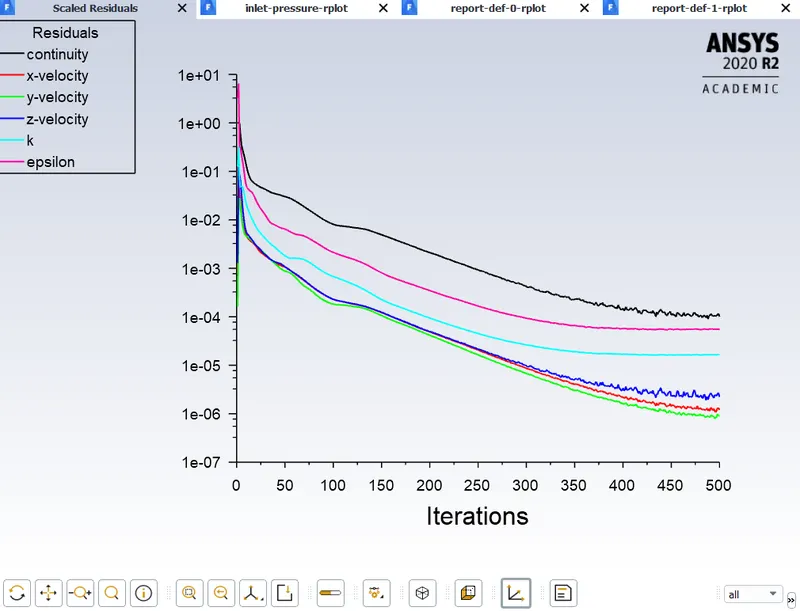
The analysis is done for 500 iterations.
- Diameter of the particles = 1 micrometer
The scaled residuals plot :
- Post-processing:
The data is exported from the fluent to CFD post to visualize the results. Opening the CFD post, the particle history data is imported.
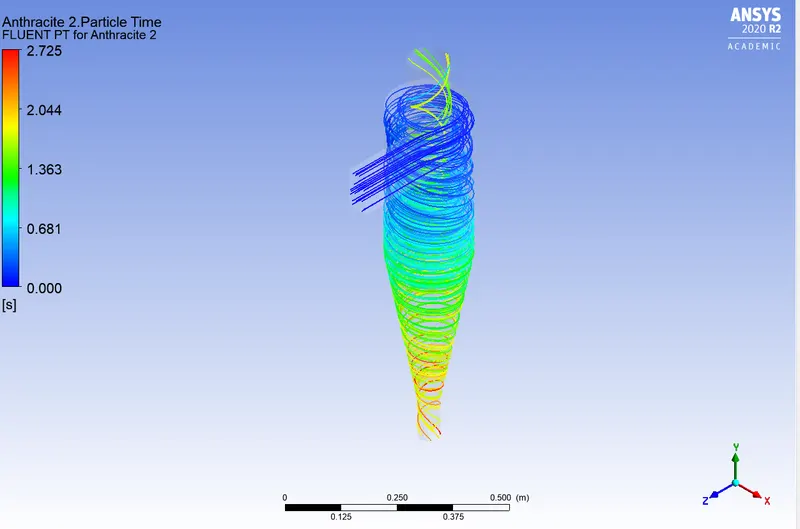
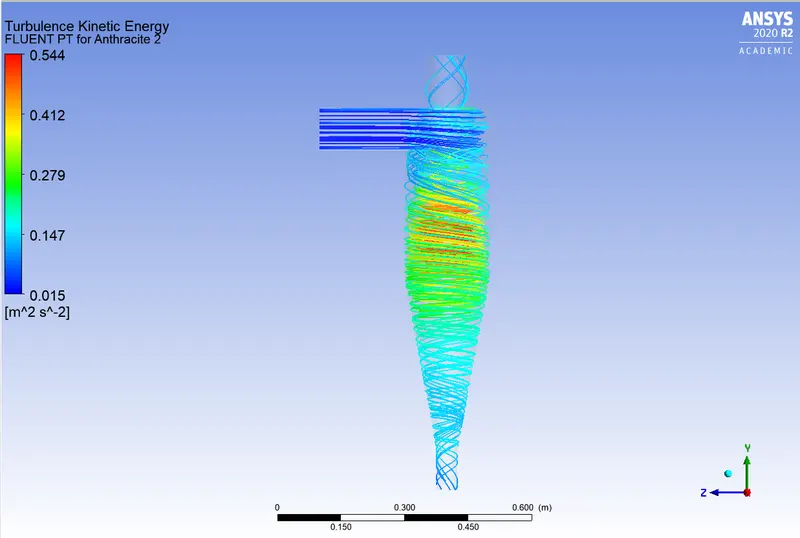
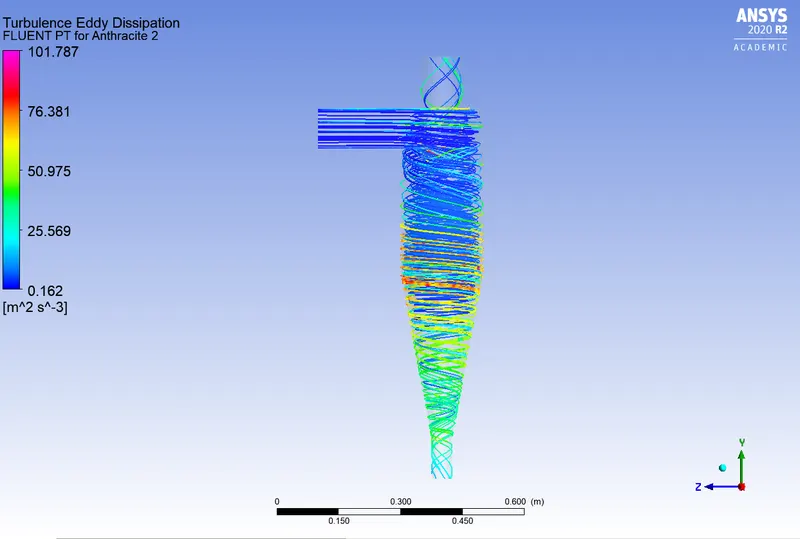
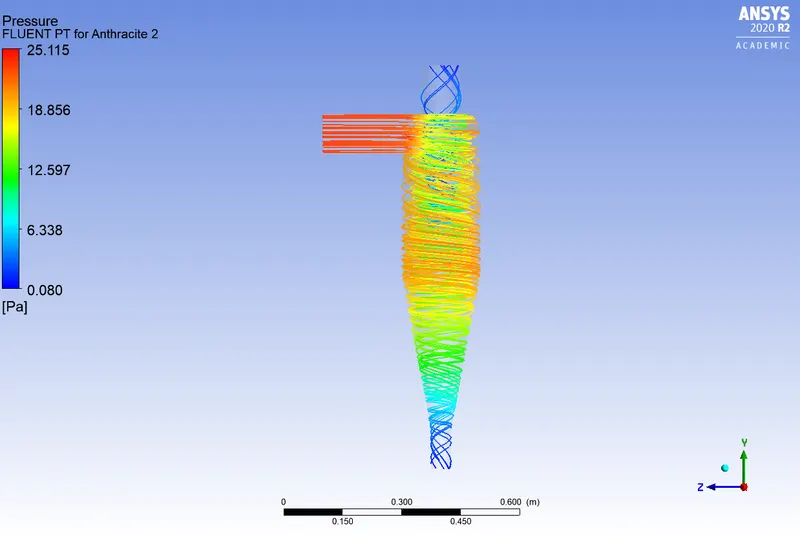
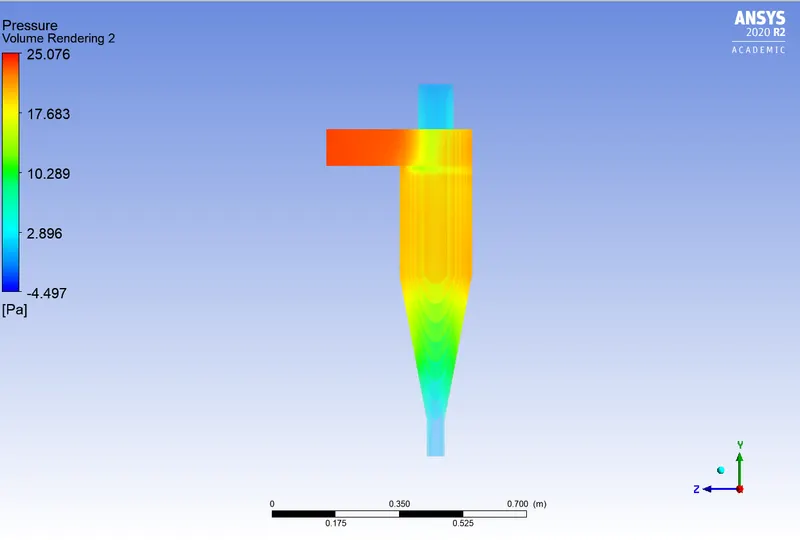
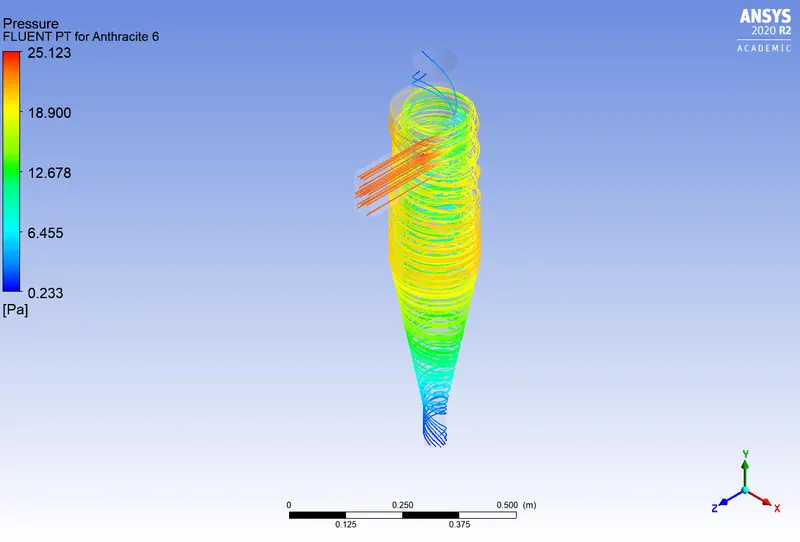
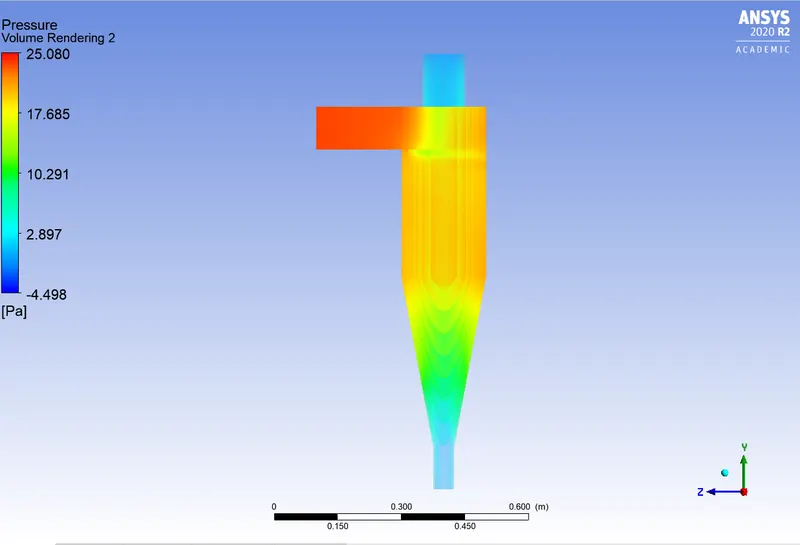
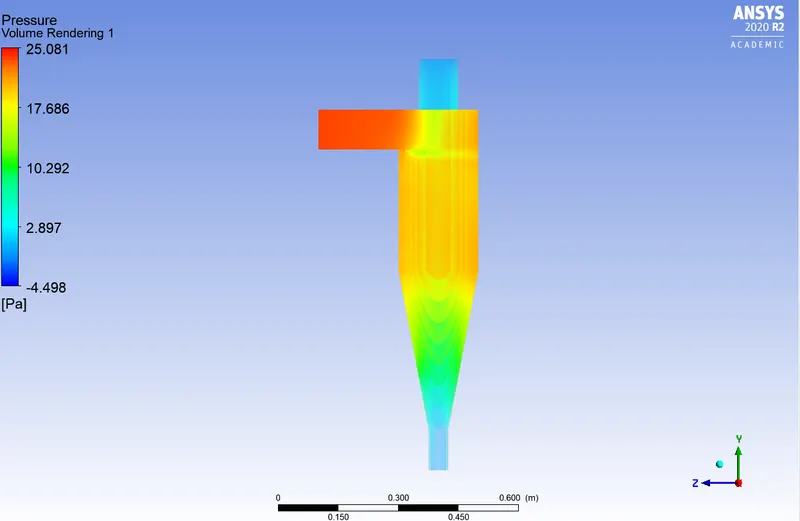
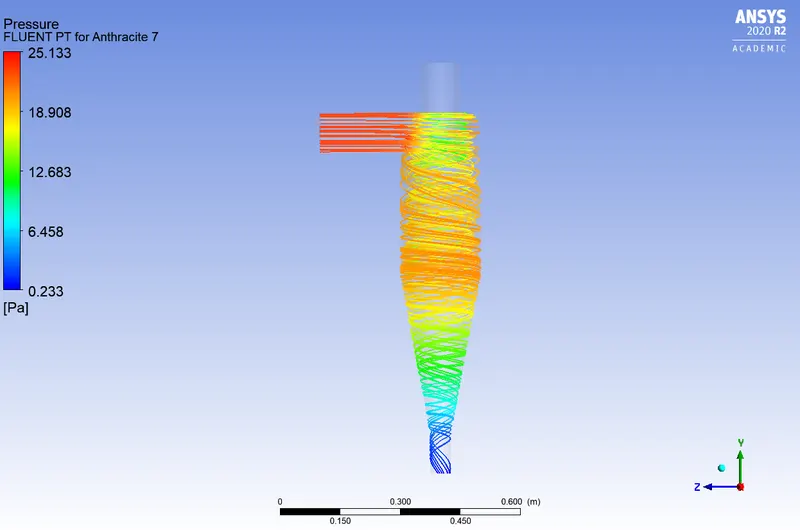
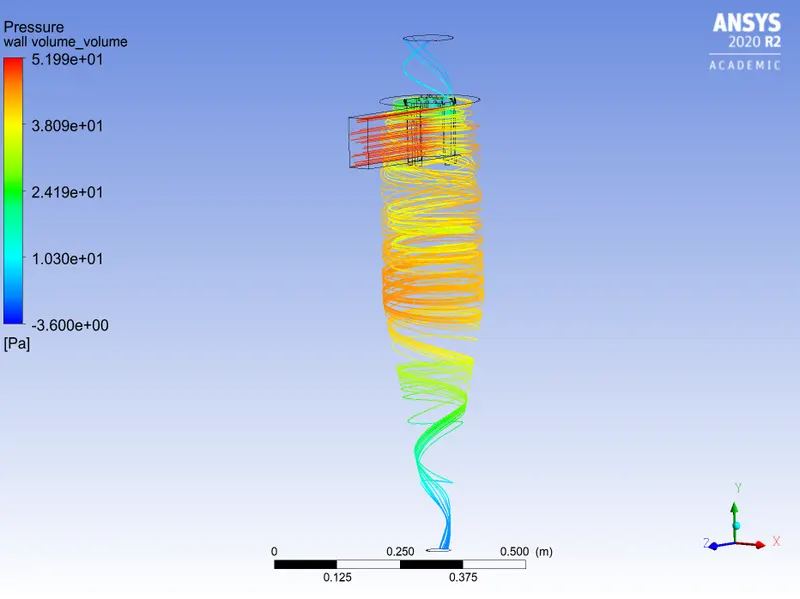
From the pressure plot, it can be inferred that the pressure is much higher at the inlets whereas it lowes at both outlets.
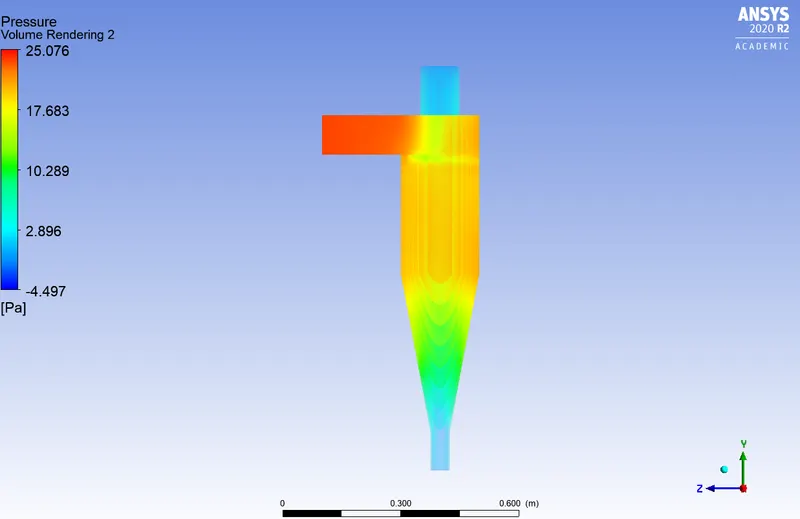
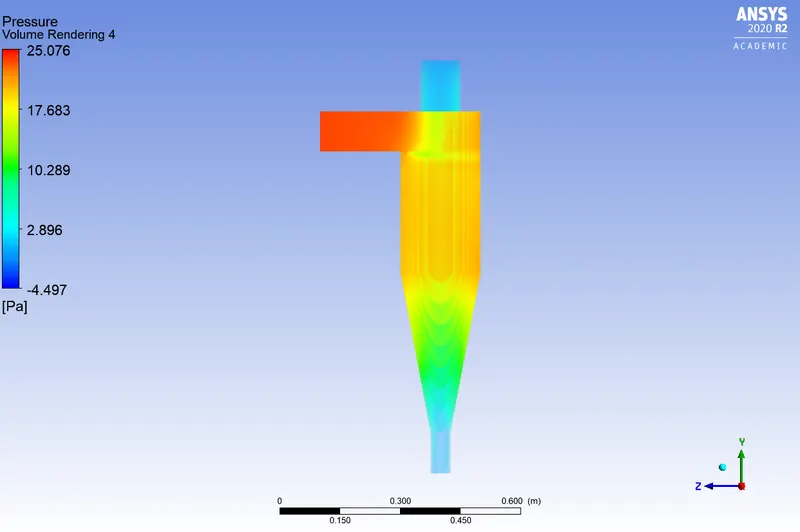
The volume can be rendered with pressure as the parameter,
| tracked | escaped | trapped | incomplete |
| 288 | 74 | 54 | 160 |
Separation efficiency:
(number of particles trapped/number of particles tracked )*100
So, separation efficiency = (54/288)*100 = 18.75%
- Diameter of the particles = 2 micrometers
The setup of the physics is the same as the above case, except the particle diameter in the DPM modeling is increased to 2 micrometers. All other boundary conditions, initialization, and solution methods are the same.
Scaled residuals :
| Tracked | escaped | trapped | incomplete |
| 288 | 57 | 191 | 40 |
Separation efficiency = (191/288)*100=66.31%
- Post-process visuals:
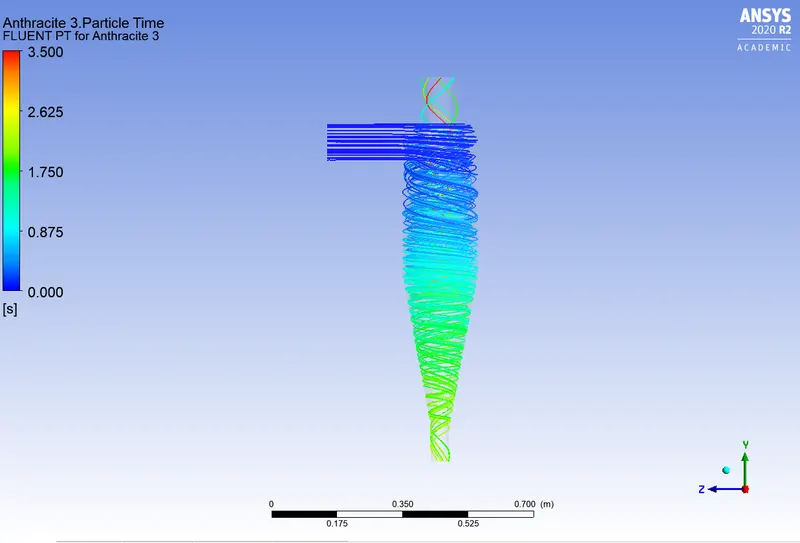
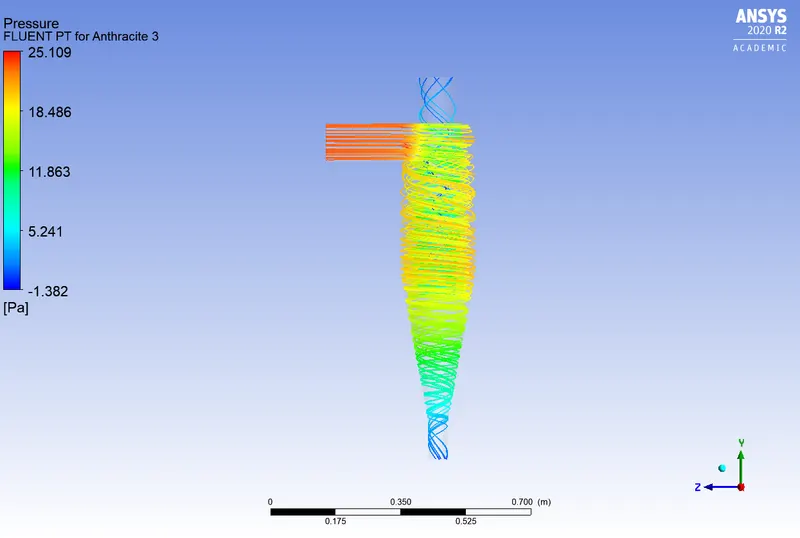
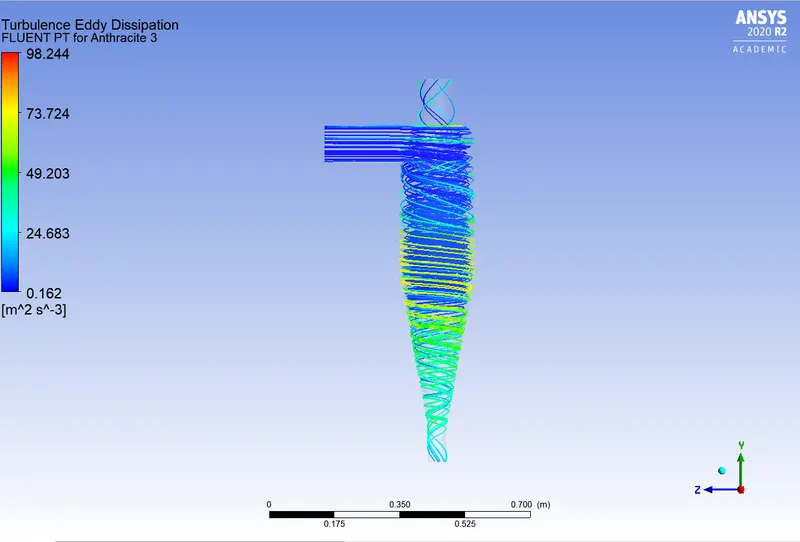
The volume rendered with pressure as variable is:
- Diameter of the particles = 3 micrometers:
The DPM interval is set to 5 iterations
| Tracked | Escaped | Trapped | Incomplete |
| 288 | 35 | 192 | 61 |
Separation efficiency= (192/288)*100 = 66.66%
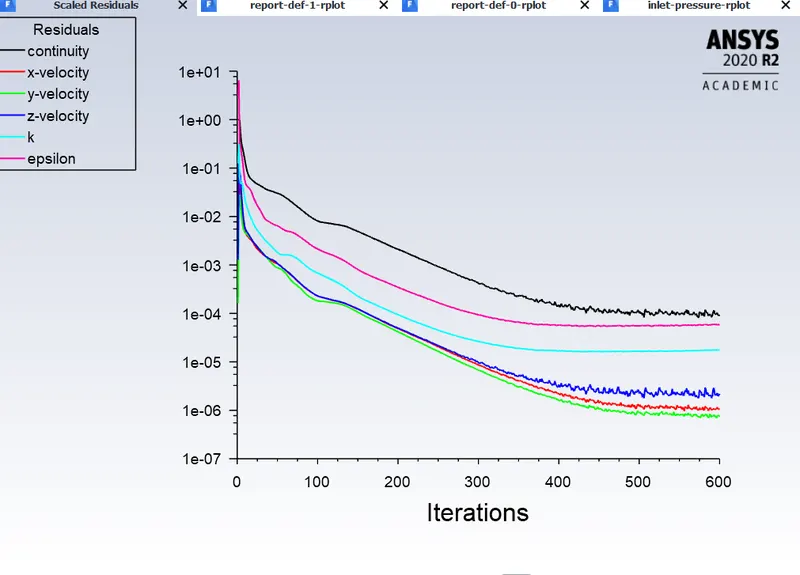
The scaled residuals are:
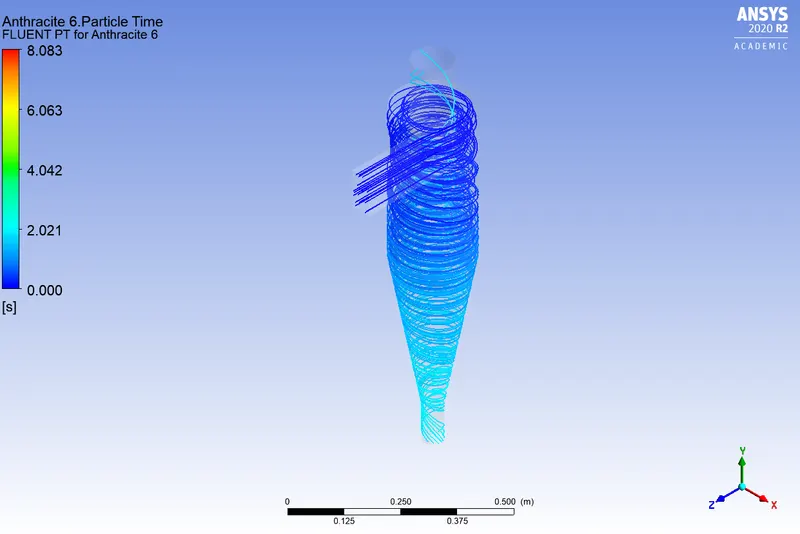
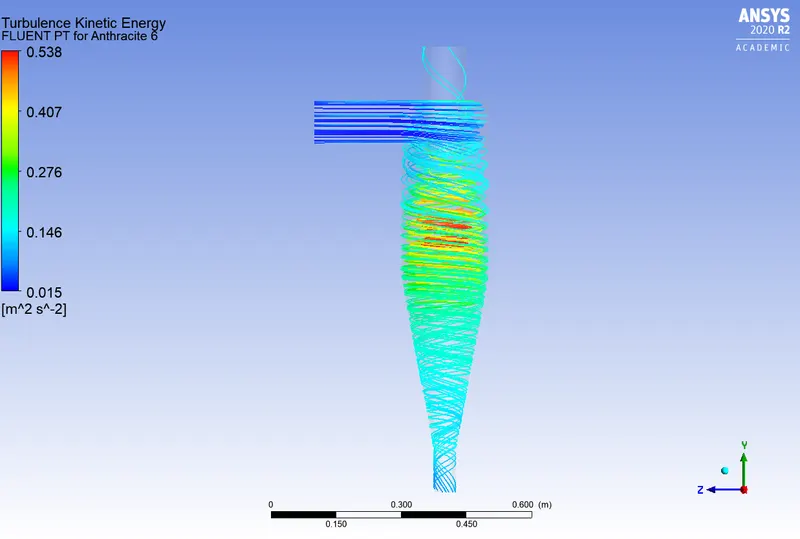
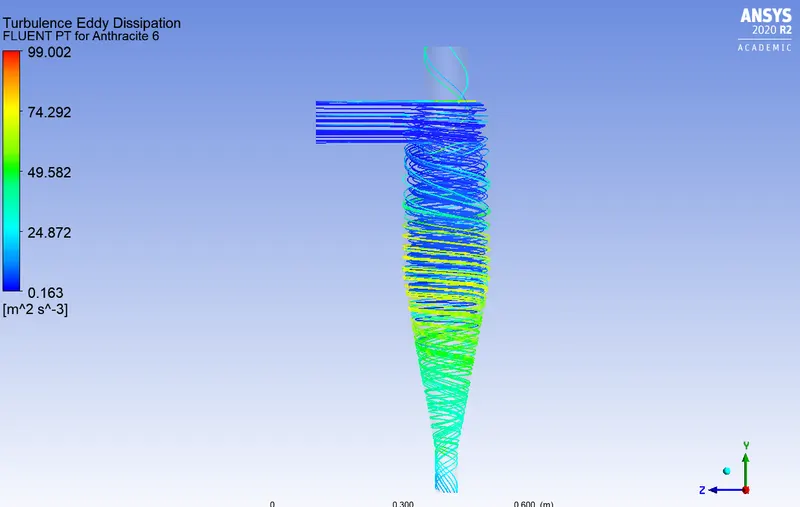
The Post processing plots of pressure, turbulent kinetic energy, turbulent eddy dissipation, volume rendering with pressure variables are:
- Diameter of the particles = 4 micrometers:
To decrease the number of particles incomplete , the DPM interval level is reduced. it is made 5.
All other parameters are same.
| Tracked | Escaped | Trapped | Incomplete |
| 288 | 7 | 219 | 62 |
Separation efficiency = (219/288)*100 = 76.04%
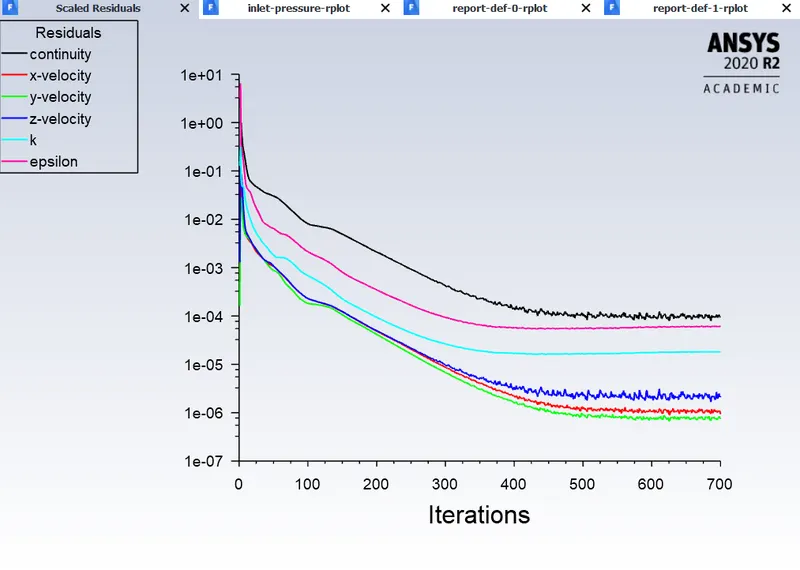
Scaled residuals:
The post processing data are:
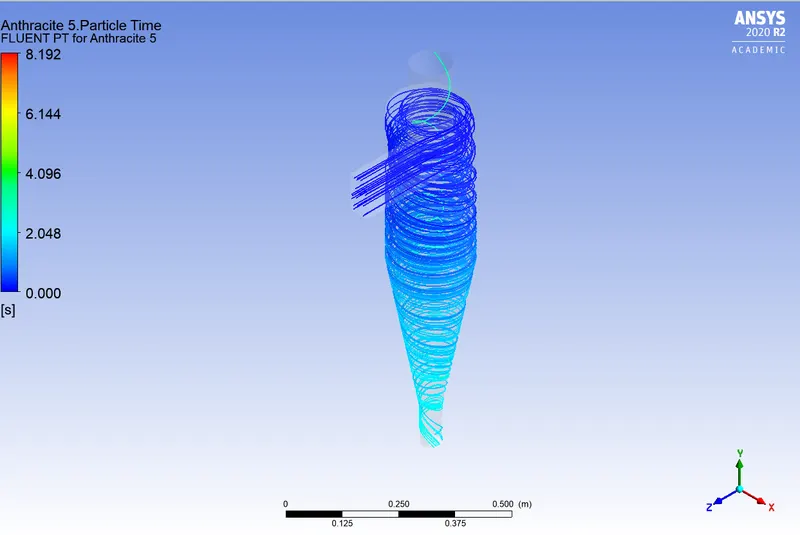
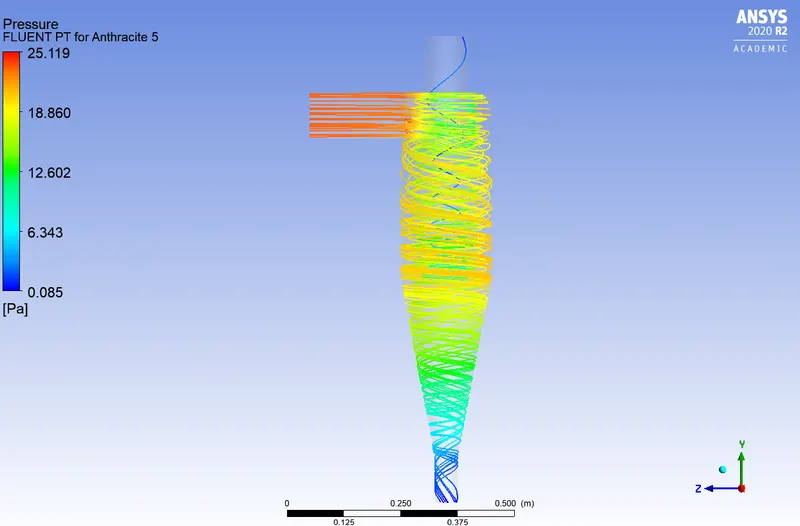
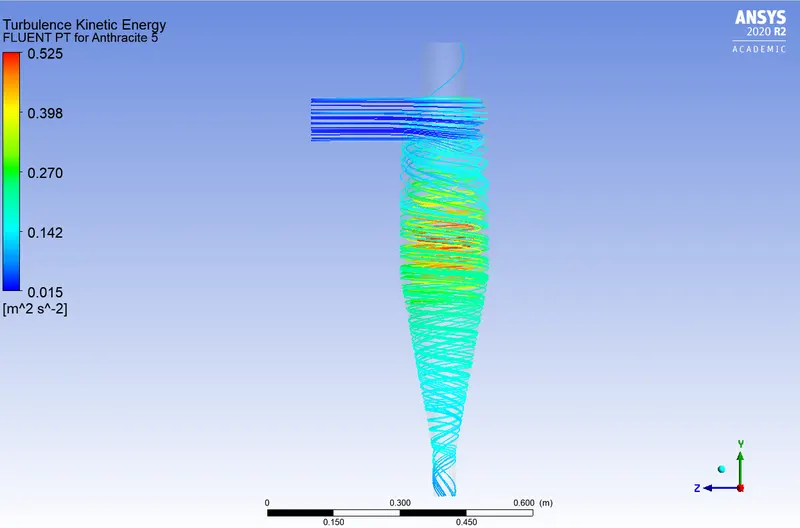
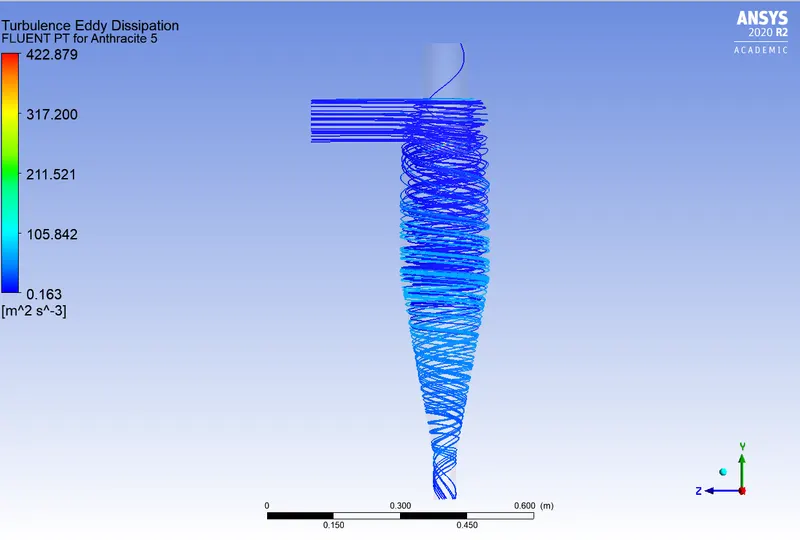
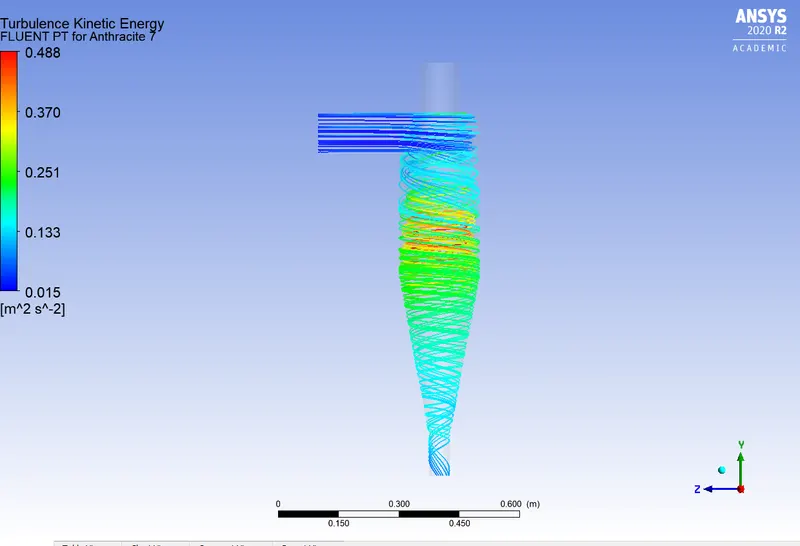
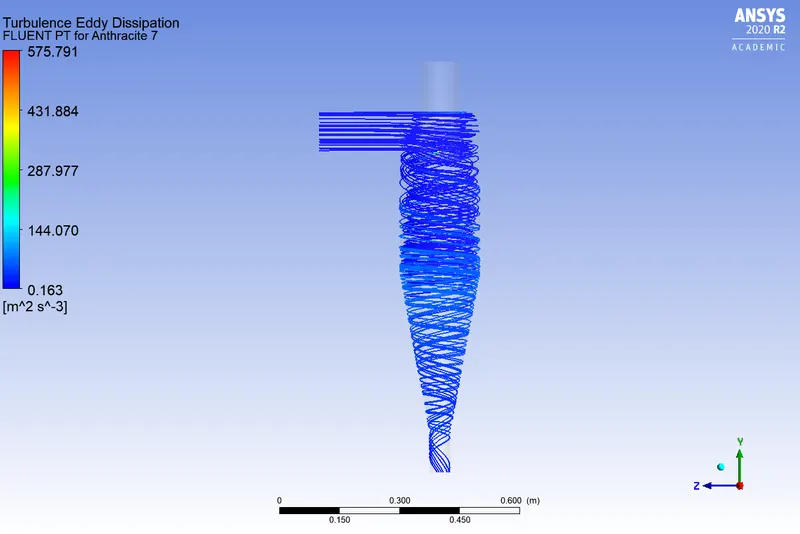
The turbulent kinetic energy and the turbulent eddy dissipation distribution is shown below.
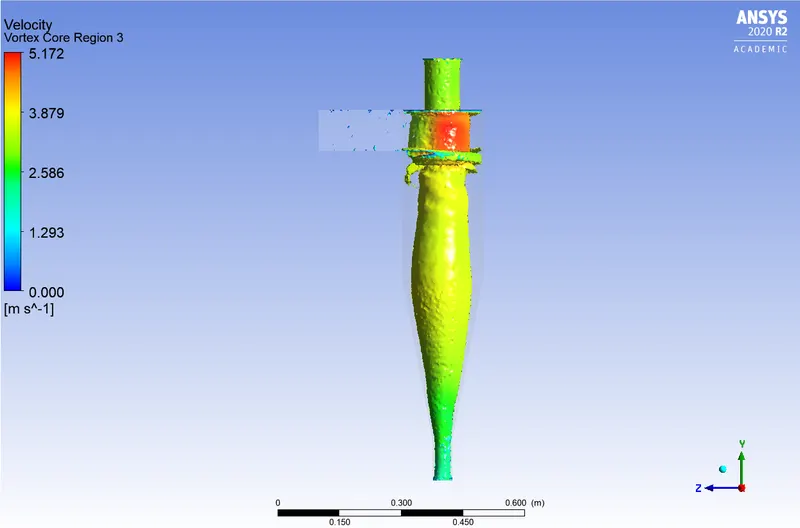
The volume rendered with pressure as variable and the velocity vortex is shown below
- Diameter of particles = 5 micrometers:
The DPM interval is set to 2 iterations.
All other conditions are same.
| Tracked | Escaped | Trapped | Incomplete |
| 288 | 0 | 267 | 21 |
Separation efficiency = (267/288)*100 = 92.70%
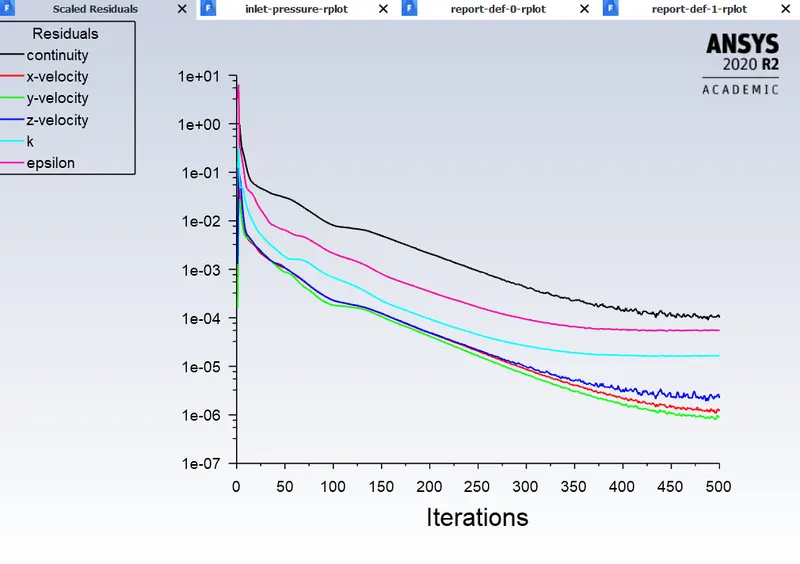
The scaled residuals are:
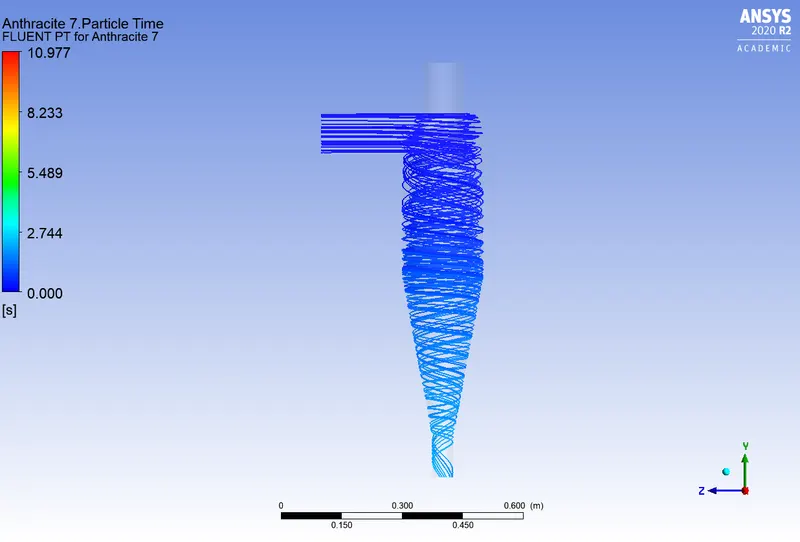
The post -processed visuals of pressure, turbulent kinetic energy, turbulent eddy dissipation, volume rendering with pressure as variable are as follows:
Vortex core region with different swirl strength :
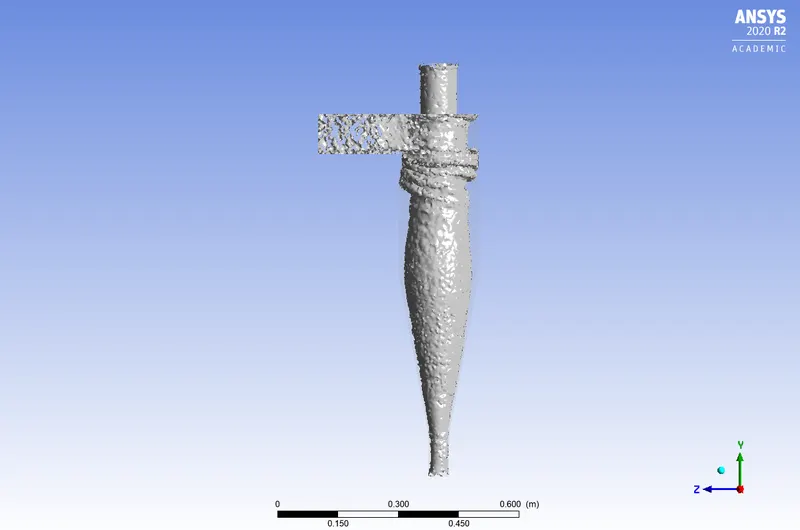 swirl strength = 0.012
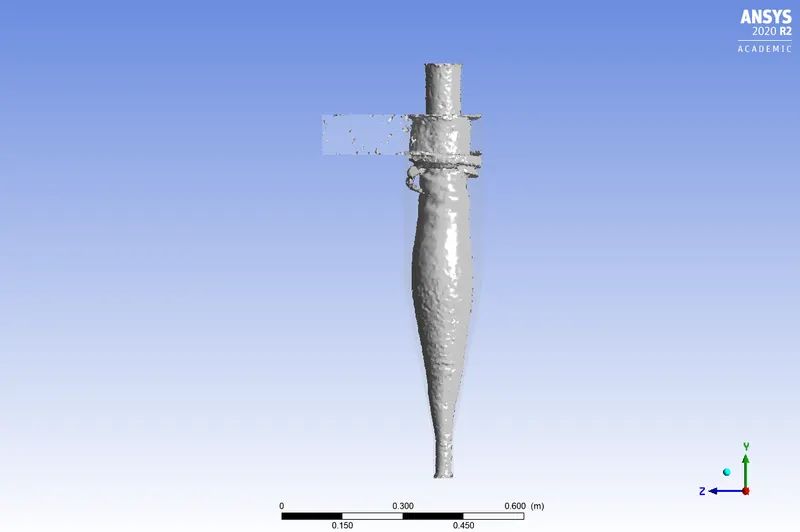 swirl strength = 0.055
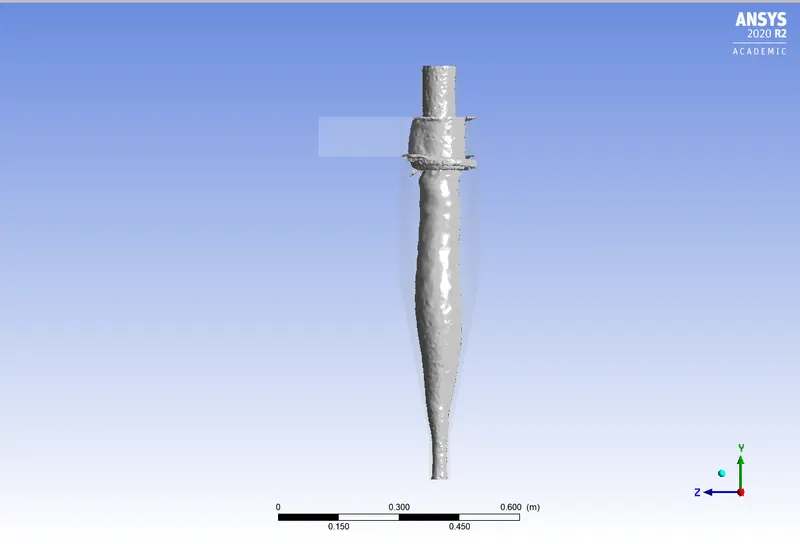 swirl stength = 0.12
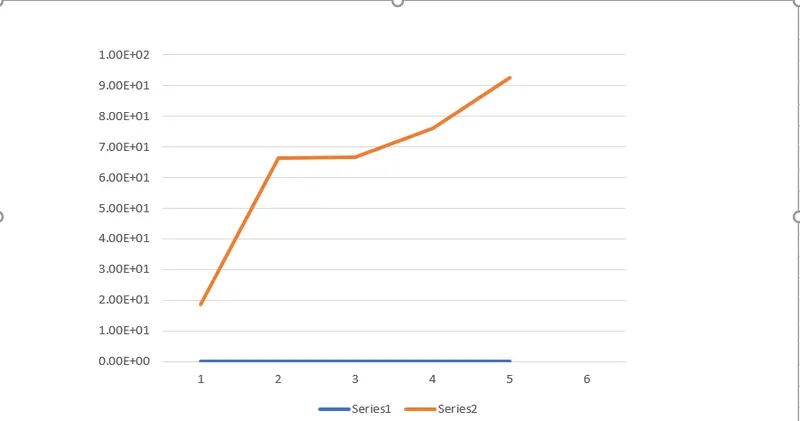
- Final efficiency tabulation:
| Particle diameter | Velocity | Efficiency(%) |
| 1e-6 | 3 | 18.75 |
| 2e-6 | 3 | 66.31 |
| 3e-6 | 3 | 66.60 |
| 4e-6 | 3 | 76.04 |
| 5e-6 | 3 | 92.70 |
- Plot of efficiency of the cyclone separator vs the diameter of the particles
The separation efficiency is plotted along the Y axis and the particle diameters along the X axis. This is done in Microsoft Excel
- Validation of results obtained by CFD analysis from the Analytical methods:
The various analytical models to calculate the separation efficiency of cyclone separators are:
1) Iozia and Leith model:
Developed from the basis of force balance. The model assumes that the particle carried by the vortex endures the influence of two forces : a centrifugal force Z and a flow resistence W. The separation efficiency can be written as :
η(i)=⎛⎜ ⎜⎝1(1+d(pc)d(p))β⎞⎟ ⎟⎠⎞⎟ ⎟⎠η(i)=(1(1+d(pc)d(p))β))
β=0.62−0.87⋅(ln(d(pc))100)+5.21⋅ln(a⋅bD2)+1.05(ln(abD2)2)β=0.62-0.87⋅(ln(d(pc))100)+5.21⋅ln(a⋅bD2)+1.05(ln(abD2)2)
d(pc)= 50% cut size
d(pc)=(9⋅μ⋅Qπ⋅ρ(p)⋅Z(c)⋅v2)0.5d(pc)=(9⋅μ⋅Qπ⋅ρ(p)⋅Z(c)⋅v2)0.5
Here Z(c) = core length and d(c) = core diameter.
Here d(c)<B;
so, Z(c) = H-S
In our model :
All dimensions are in meters.
D(e)=0.1
D=0.2
b=0.05
a=0.1
h=0.4
H=0.8
B=0.05
Rho=1550 kg/m^3
mass flow rate = 1e-20
Calculating Q = mass flow rate * Rho
And putting the values in the equation of efficiency, we get , separation efficiency = 98%
error = (98-92.70)/98 *100 =5.40 %
The efficiency can be increased by increasing the number of cells in the mesh.
2)Koch and Licht model:
Koch and Licht inherently described the turbulent nature of cyclones and distribution of gas residence times within the cyclone. They attributed by the two following assumptions:
- The tangential velocity of the particle is equal to the tangential velocity of the gas flow. There is no slip in the tangential direction between gas nad particle.
- The tangential velocity is related to the radius of the cyclone by uR^n = constant
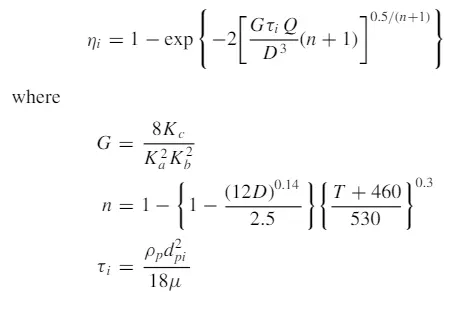 This is the formula for the grade efficiency
3) Li and Wang model:
-
The Li and Wand model include particle bounce or re-entrainment and turbulent diffusion at the cyclone wall. A two-dimensional analytical expression of particle distribution in the cyclone is obtained. Li and Wang's model was developed based on the following assumptions:
1. The radial particle velocity and the radial concentration profile are not constant for uncollected particles within the cyclone.
2. Boundary conditions with the consideration of turbulent diffusion coefficient and particle bounce re-entrainment on the cyclone wall are:
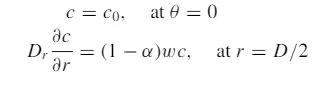
- The tangential velocity is related to the cyclone radius by uR^n=constant
The concentration distribution is given as :
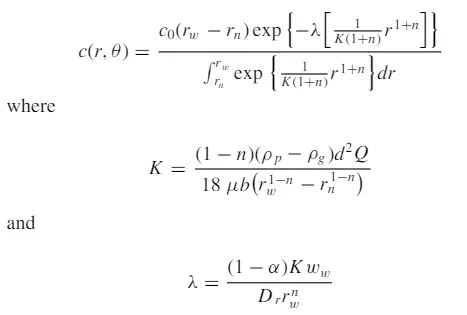
The expression for collection efficiency for particles of any size is given as:
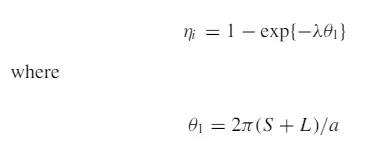
Lapple Model:
Lapple model was developed based on force balance without considering the flow resistance. Lapple assumed that a particle entering the cyclone is evenly distributed across the inlet opening. The particle that travels from the inlet half-width to the wall in the cyclone is collected with 50% efficiency. The semi-empirical relationship developed by Lapple to calculate a 50% cut diameter, dpcdpc is
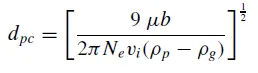
where NeNe is the number of revolutions
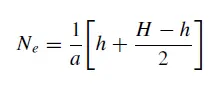
The efficiency of collection of any size of the particle is given by
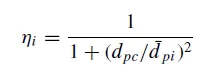
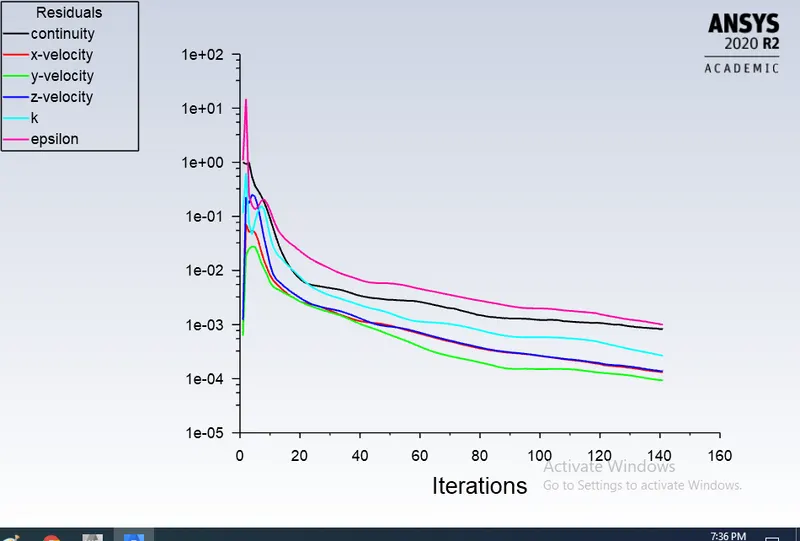
- Manipulation of the inlet velocity from 1m/s to 5m/s for a fixed particle diameter :
inlet velocity=1m/s,Dia of particle=5e-6
Residual:
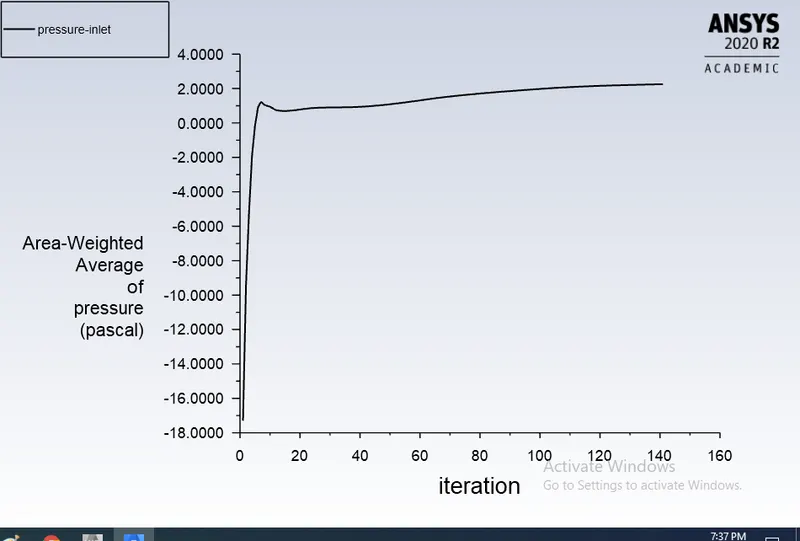
Pressure inlet:
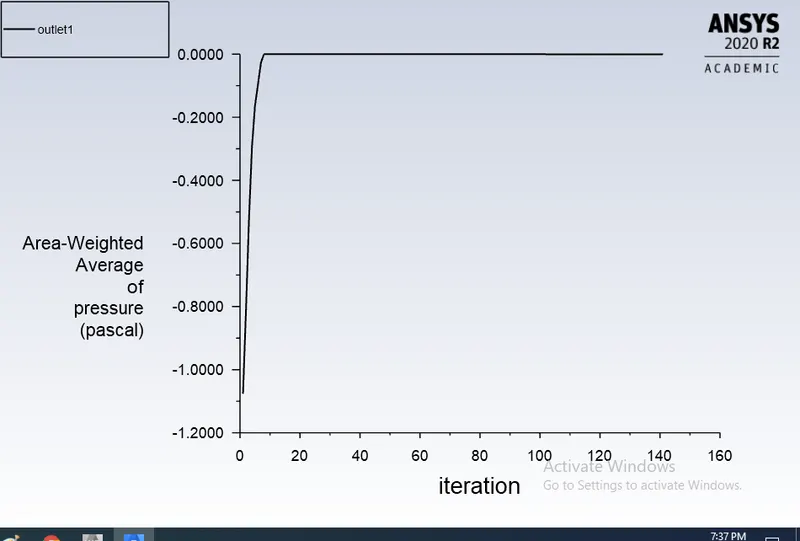
Pressure outlet(Top):
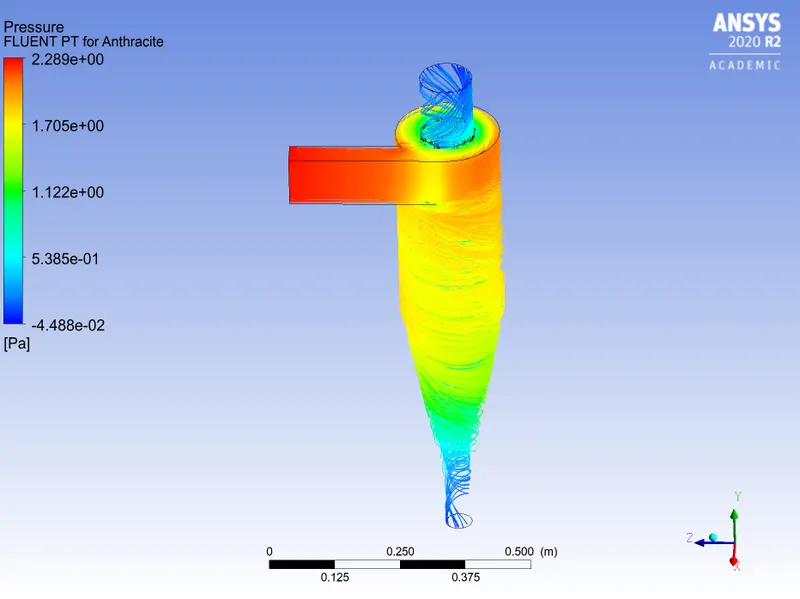
Contour:
Values of pressure inlet/outlet:
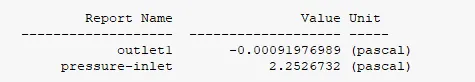
Pressure drop=inlet-outlet
=2.2526732-(-0.00091976989)
=2.2535
DPM:

Cyclone separator efficiency:
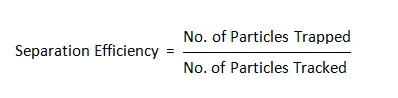
= (14/378)*100
= 3.7%
inlet velocity=2m/s,Dia of particle=5e-6
Residual:
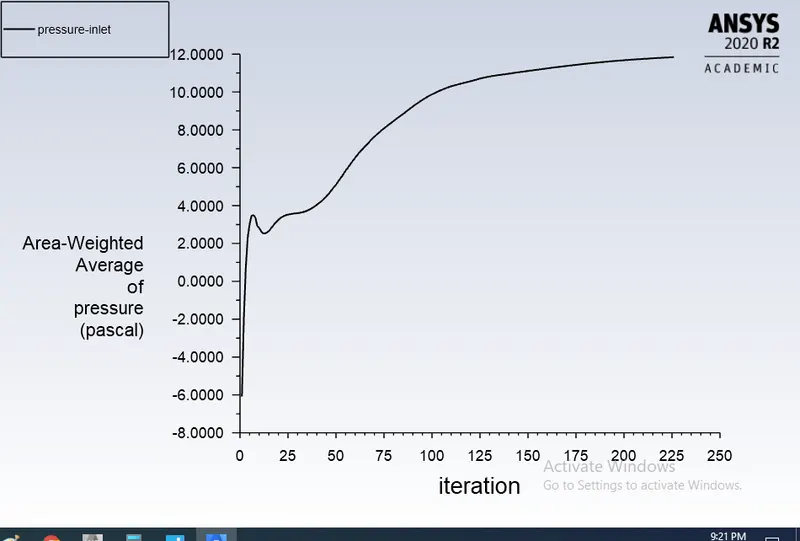
Pressure inlet:
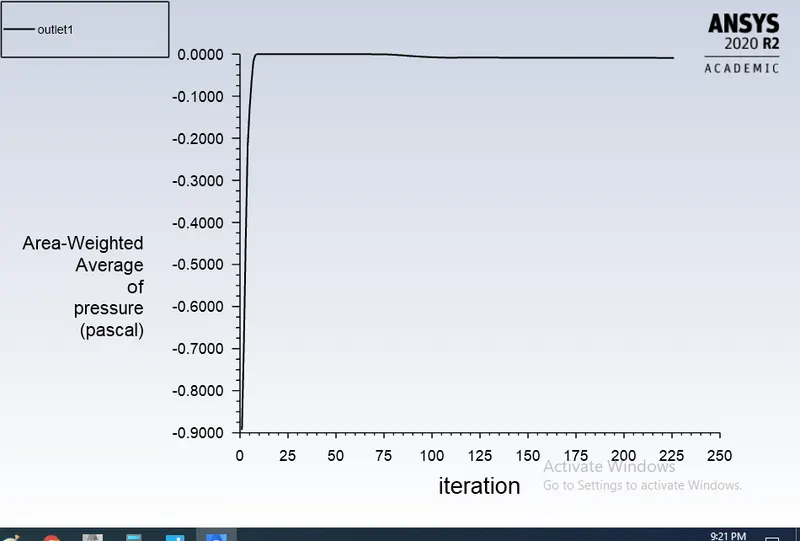
Pressure outlet:
Contour:
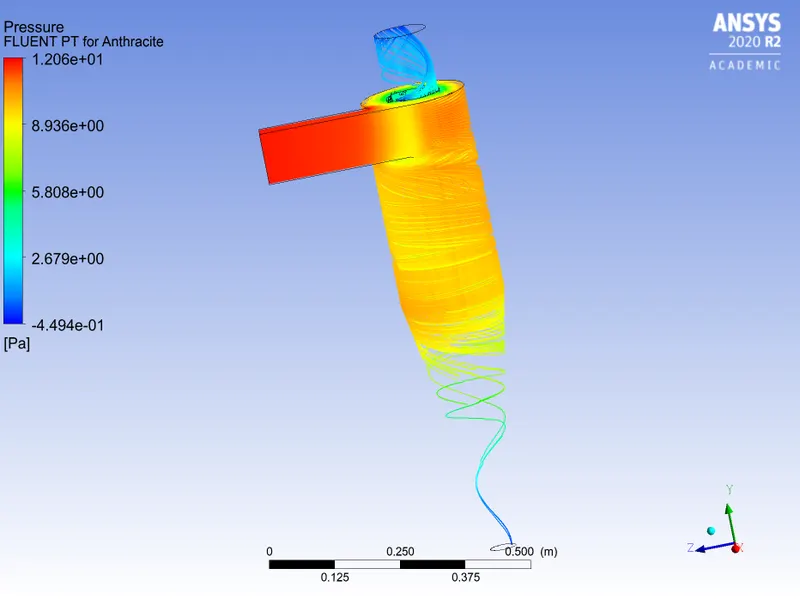
Values of pressure inlet/outlet:
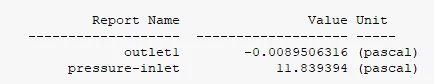
Pressure drop=inlet-outlet
=11.839394-(-0.00895)
=11.848343
DPM:

Cyclone separator Efficiency:
Efficiency=(4/378)*100
=
inlet velocity=3m/s,Dia of particle=5e-6
Residual:
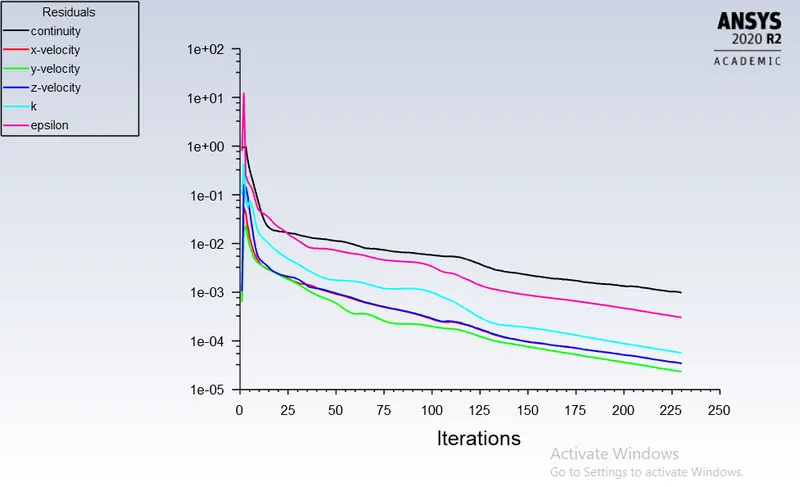
Pressure outlet: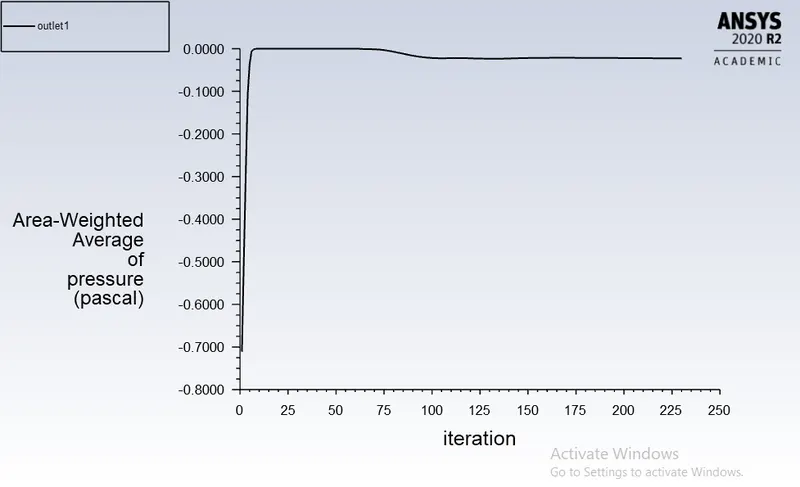
Pressure inlet:
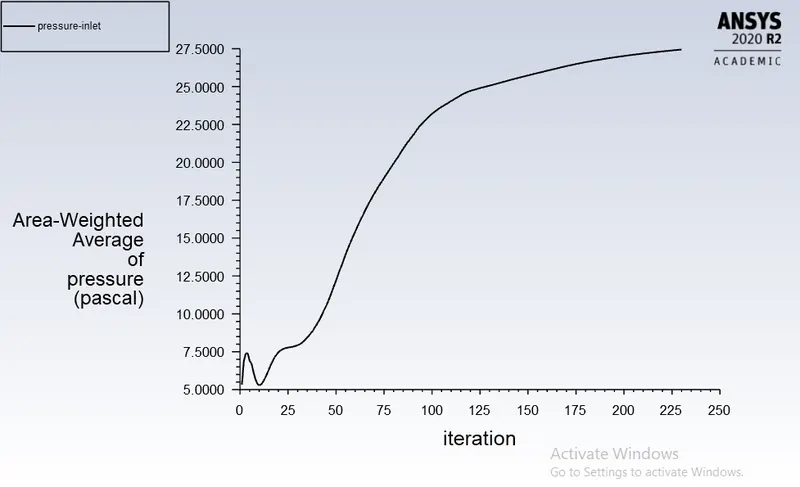
Pressure drop: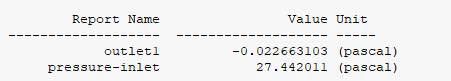
Pressure drop=Inlet-Outlet
= 27.442011-(-0.022663)
= 27.46
DPM:
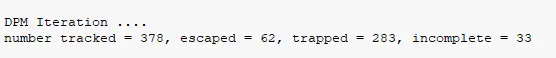
Cyclone separator Efficiency:
Efficiency= (283/378)*100
= 74.86%
inlet velocity=4m/s,Dia of particle=5e-6
Residual:
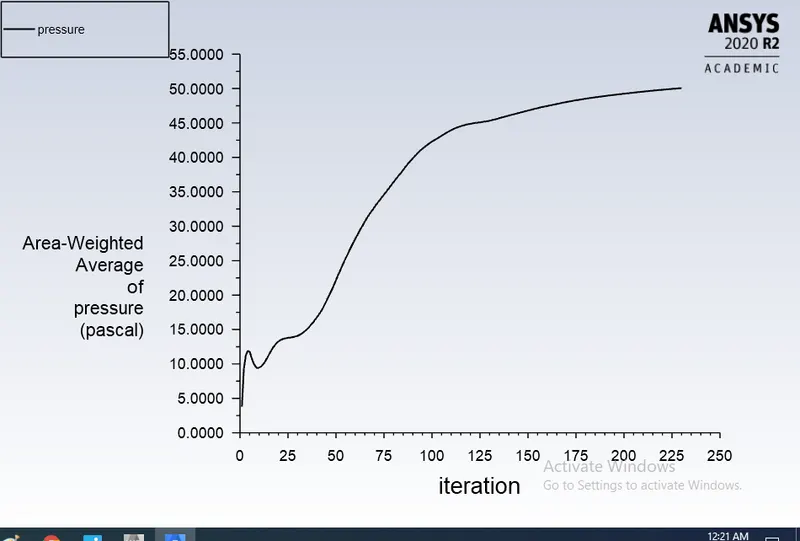
pressure inlet:
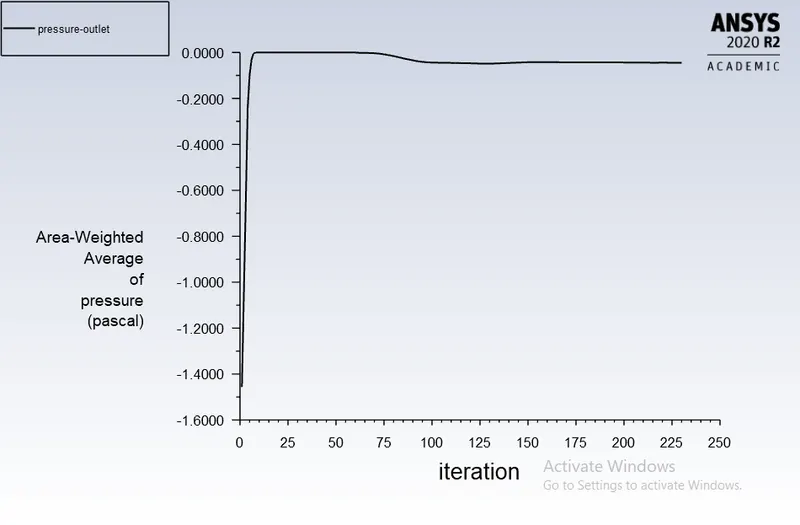
Pressure outlet:
Contour:
Pressure drop:
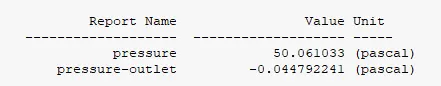
Pressure drop=Inlet-outlet
= 50.061033-(-0.044792241)
= 50.1058
DPM:
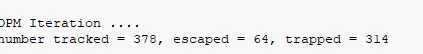
Cyclone separator Efficiency:
Efficiency = (314/378)*100
=83.37%
inlet velocity=5m/s,Dia of particle=5e-6
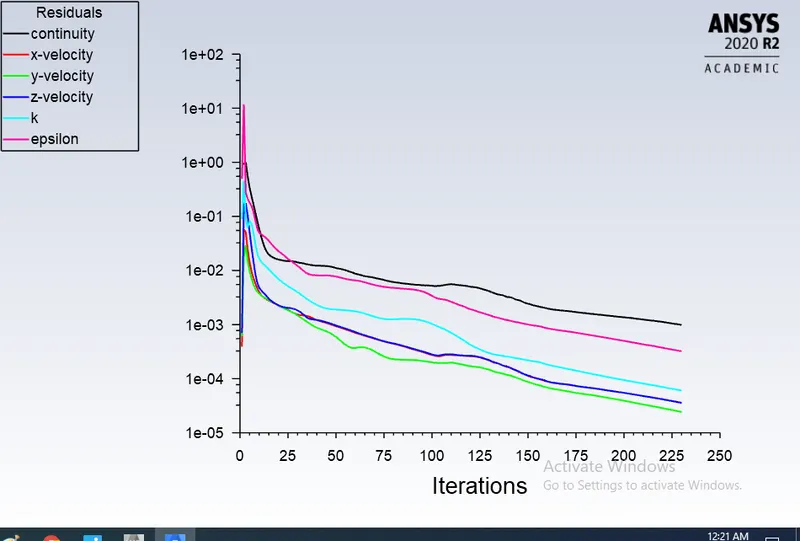
Residual:
Inlet:
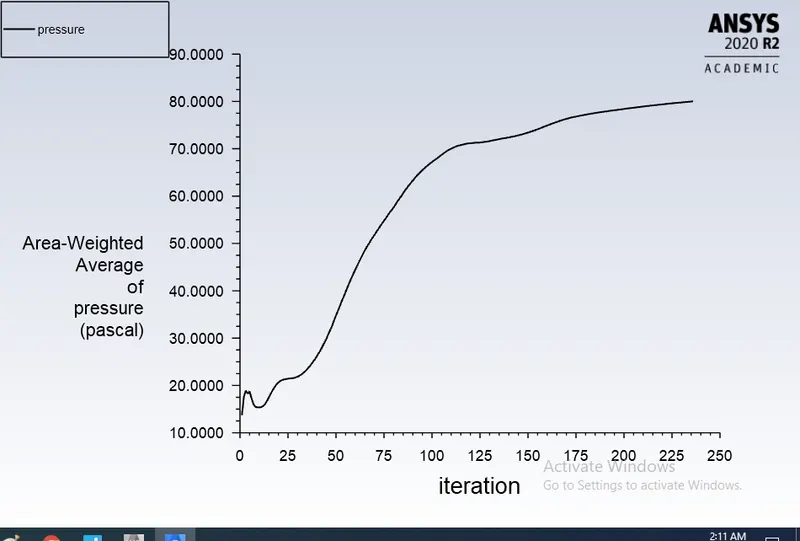
Outlet:
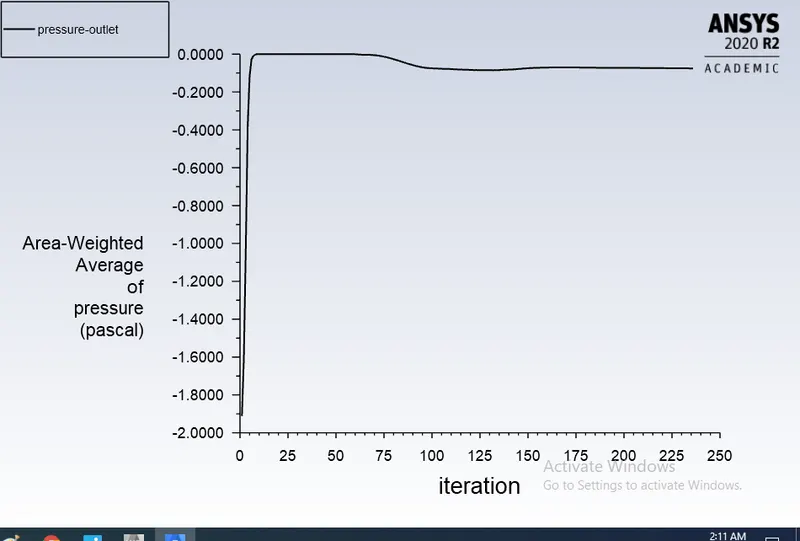
Contour:
Pressure drop:
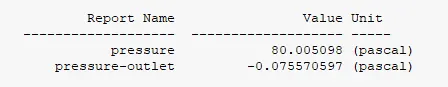
Pressure drop=Inlet-Outlet
=80.005098-(-0.075570597)
=80.08
DPM:
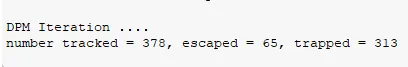
Cyclone separator Efficiency:
Efficiency = (314/378)*100
= 83.06%
- Separation efficiency:
It is defined as the fraction of particles of a given size collected in the cyclone, compared to those of that size going into the cyclone. Experience shows that the separation efficiency of the cyclone separator increases with increasing particle mean diameter and density; increasing gas tangential velocity; decreasing cyclone diameter; increasing cyclone length; extraction of gas along with solids through the cyclone legs.
In this case, depending on the particle history data - Separation Efficiency is defined as the ratio of concentration that has been removed from the feed stream to the initial concentration in the feed stream. For this case ratio of the number of trapped particles to the total number of particles tracked.
Separation efficiency = no. of particles trapped / no. of particles tracked
- Pressure Drop:
Pressure drop across the cyclone is of much importance in a cyclone separator. The pressure drop significantly affects the performance parameters of a cyclone. The total pressure drop in a cyclone will be due to the entry and exit losses, and friction and kinetic energy losses in the cyclone. Normally the most significant pressure drop occurs in the body due to swirl and energy dissipation.
Pressure drop is defined as the difference in total pressure between two points of a fluid-carrying network.
Pressure drop, ΔPΔP = Total inlet pressure - Total Outlet Pressure (escape)
As the escape DPM condition is given to the outlet-top in this case, so outlet-top is considered in the pressure drop calculation.
Part 2
- Final efficiency and pressure drop tabulation:
| Part-2 | Size of particle(m) | Velocity of particle(m/s) | Particle tracked | Particle trapped |
Particle Escaped |
Separator efficiency | pressure drop |
| B1 | 5e-6 | 1 | 378 | 14 | 81 | 3.7 | 2.235 |
| B2 | 5e-6 | 2 | 378 | 7 | 61 | 11.85 | 11.84 |
| B3 | 5e-6 | 3 | 378 | 283 | 62 | 74.8 | 27.46 |
| B4 | 5e-6 | 4 | 378 | 313 | 84 | 82.8 | 50.10 |
| B5 | 5e-6 | 5 | 378 | 314 | 65 | 83.8 | 80.08 |
Inference:
From the above pressure velocity plots, we can infer that the pressure is higher near the wall region which forms the outer vortex. Due to higher pressure near the wall low-pressure region is created at the center of the cyclone separator because of which the lighter particles escape from the top outlet and heavier particles are collected at the bottom outlet.
simulation is done for particle size varying from 1μμm to 5μμm with air and particle velocity as 3m/s. From the video, it is observed that heavier particle is trapped at the bottom outlet and lighter particles are escaped at outlet 1. But we can also see that lighter particles also get trapped at the bottom outlet because of interaction between lighter and heavier particles and there is an exchange of inertial forces between them as a result there is a transfer of Kinetic energy from heavier particles to the lighter particle, as a result, we can observe a certain number of heavier particles escapes through the top outlet.
The collection efficiency of cyclones varies as a function of particle size, density, and cyclone design. Cyclone efficiency will generally increase with the increase in particle size, density, inlet duct velocity, cyclone body length, number of gas revolutions in the cyclone, the ratio of cyclone body diameter to gas exit diameter, inlet dust loading, smoothness of the cyclone inner wall.
The efficiency of the cyclone will decrease with an increase in the parameters such as gas viscosity, cyclone body diameter, gas exit diameter, gas inlet duct area, gas density, and leakage of air into the dust outlet.
With the increase in inlet velocity or particle size the efficiency increases.
The collection efficiency of the cyclone separator is related to the pressure drop across the cyclone. Here pressure drop is the indirect measure of the energy required for the gas to move the particles. Pressure drop is related to the inlet velocity of air and particle size.
Pressure drop occurs because of the following components:
1. Loss due to the expansion of gas in the cyclone chamber.
2. Loss due to rotational kinetic energy.
3. Loss due to wall frictional forces