Week 8 - Challenge 6 - Core & Cavity Design
Switch Bezel Design
Introduction
Create the Switch Bezel Plastic component through the given Class-A surface. To begin with, the tooling axis for the given Class-A Surface should be created meeting the requirements of the draft angle and at the end perform the Draft analysis on the model and create the Core and cavity blocks for the switch bezel designed in the earlier challenge.
Tooling axis Creation
In injection molding, the Class A surface is first analyzed to determine the axis or tooling direction that separates the molds. Tooling direction is critical for plastic product design because it determines mold direction
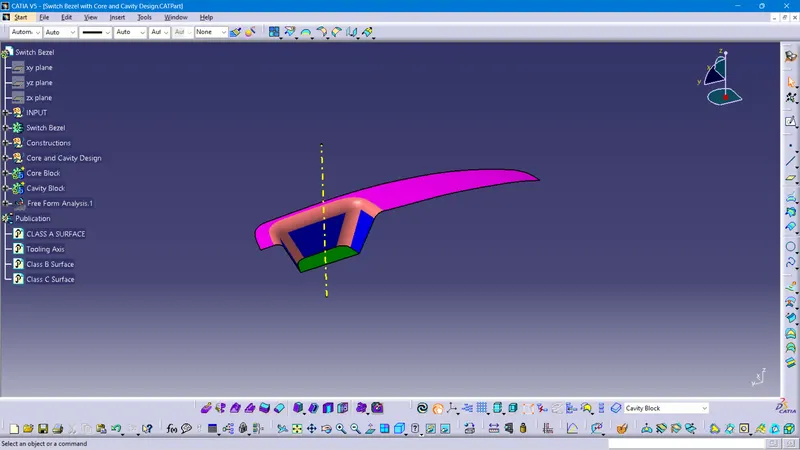
What is Draft Analysis?
Draft Analysis
For molded or cast parts, the draft angle is the amount of taper perpendicular to the parting line. It is measurable in degrees. Because plastic shrinks and sticks on molding surfaces as it cools, we draft the walls of the plastic part so that it ejects or breaks free from the molding surfaces more easily and without dragging. To reduce the risk of damage to the parts and ensure ejection, a functional injection molding part must have drafts on both the cavity and core sides.
Nominal values for Draft angles
- 3 Degrees is a nominal draft angle
- 5 Degrees can also be manufactured. Increasing the manufacturing cost
- 7 Degrees is considered for Textured surface parts
Importance of Draft in injection molding
- Reduces the possibility of part damage due to friction during the release
- Reduces mold wear and tear
- Ensures a uniform, smooth, unscratched finish
- Ensures the integrity and uniformity of other surface finishes and textures
- Reduces overall cooling time by reducing or eliminating the need for unusual ejection setups
Steps followed for Draft Analysis
- The created part must be changed to the material mode in the display frame
- Compass is enabled and placed in the direction of the Tooling Axis
- The lock command is then used to fix the compass along the tooling axis
- Colour codes are classified and a Draft angle is applied
- Running point analysis is used to display permissible draft angle
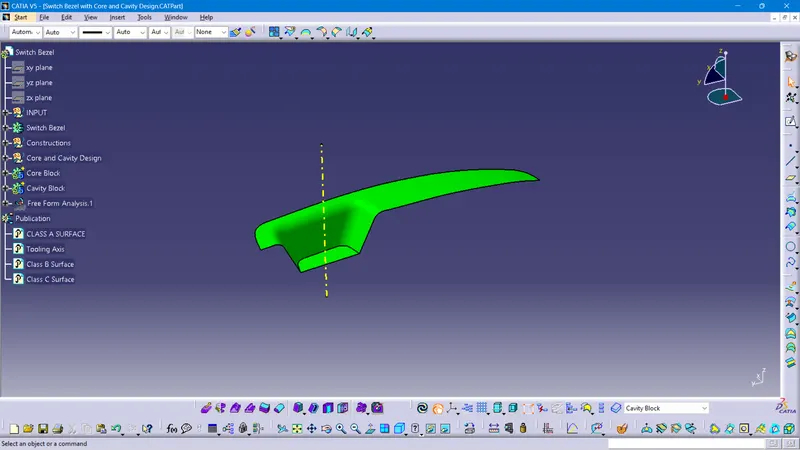
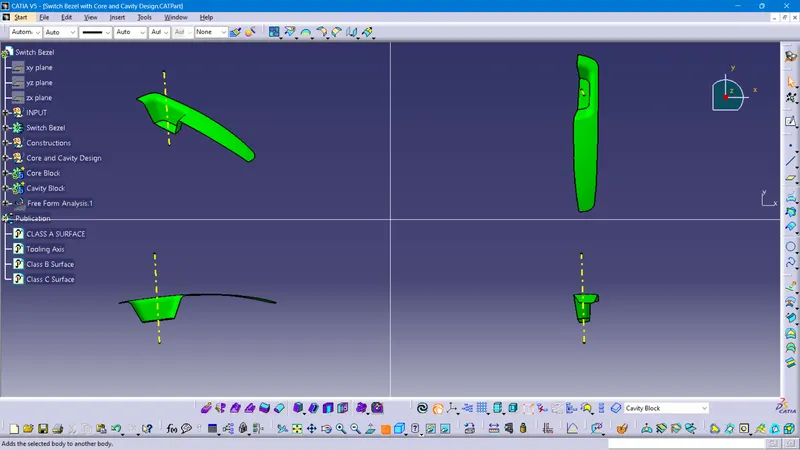
Input given: class A surface
Creation of Class B Surface
It is the offset surface of the Class A Surface the offset value depends on the thickness of the material, here the offset value is 2.5mm
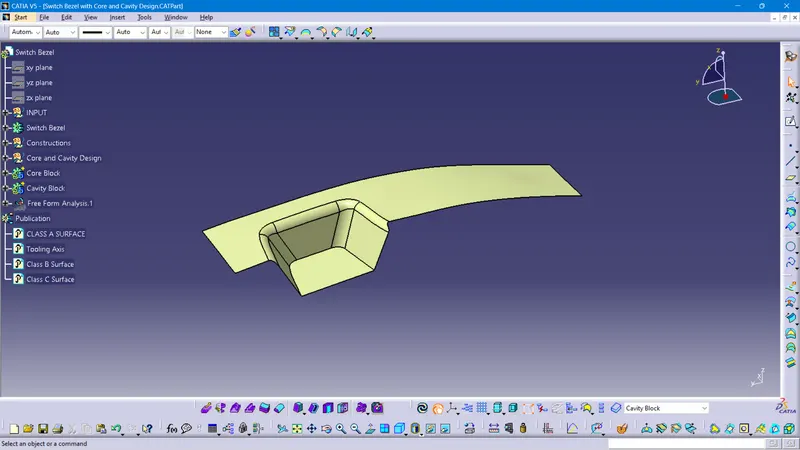
Class C surface
The surface that Joins both Class A and Class B surfaces is considered to be Class C Surface
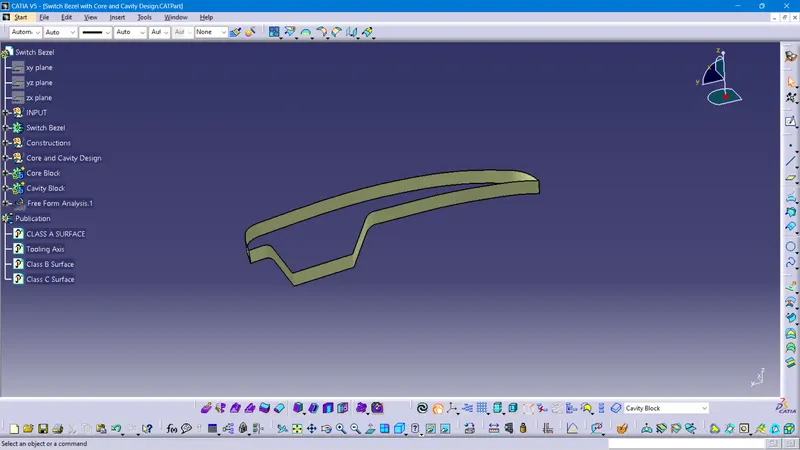
Class (A+B+C)
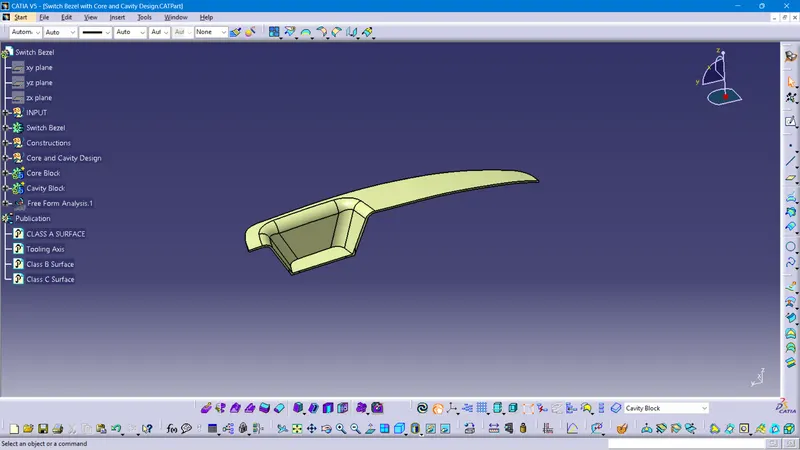
Here we combine all the surfaces into one closed surface using the Trim tool Command
Conversion of Closed surface into Solid Part
Using Solid Command, we convert the closed surface to a solid surface in the Part model
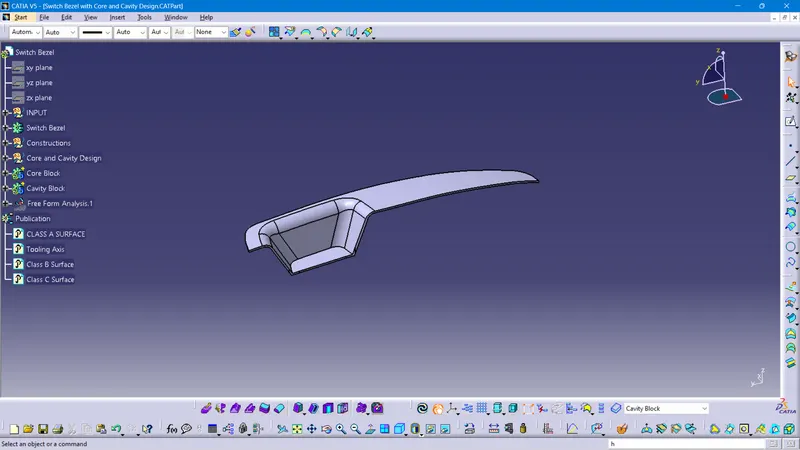
Core and Cavity Design
The core & cavity are the shaped sections in either half of the mold tool which give the plastic product its final shape. The hot molten material is injected into the core & cavity and then sets hard into shape. The design of the core & cavity is essential in the correct formation of the product.
A core is a preformed, bonded, sand insert placed into the mold to shape the interior of a casting or a part of the casting that cannot be shaped by the pattern. Cores are frequently used to create hollow sections or cavities
Core (B Side): The core is usually the interior or noncosmetic side of the part. The core side also contains the ejection mechanism that pushes the completed part out of the mold. Cavity (A Side): The cavity is the void inside the mold that the molten plastic fills.
Cavity and core are used in the injection molding process, where the concave part of the mold is the cavity and the convex part is the core.
The cavity and core are used in pairs, with the cavity also referred to as the female mold and the core as the male mold.
These two mold components are the most important parts of a mold.
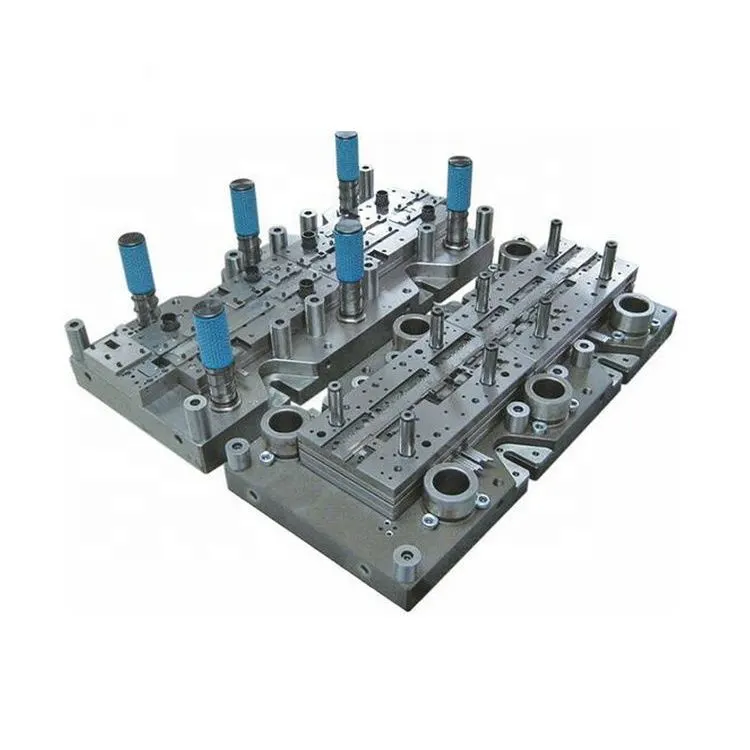
The parting surface of a mold is those surfaces of both mold plates adjacent to the impressions which butt together to form a seal and prevent the loss of plastic material from the impression. A parting line, in the industrial casting of molds, is borderline in which draft angles change direction. One can check the parting line in the mold or product which divides the two halves, i.e; the core and the cavity of a molded part. It is sometimes a starting point for the mold parting surface. In engineering drawing, a parting line is often abbreviated as PL. ASME's Y14.8 standard specifies a symbol for parting lines. Engineering applications (seals, tight-running molded parts) that require precision for shape control, call for the removal of flashes. Many molders will repair or even replace the mold tooling so that the flash is reduced to an acceptable tolerance or eliminated. Secondary operations to remove parting line flash include hand trimming, vibratory tumbling, media blasting, and cryogenic deflashing.
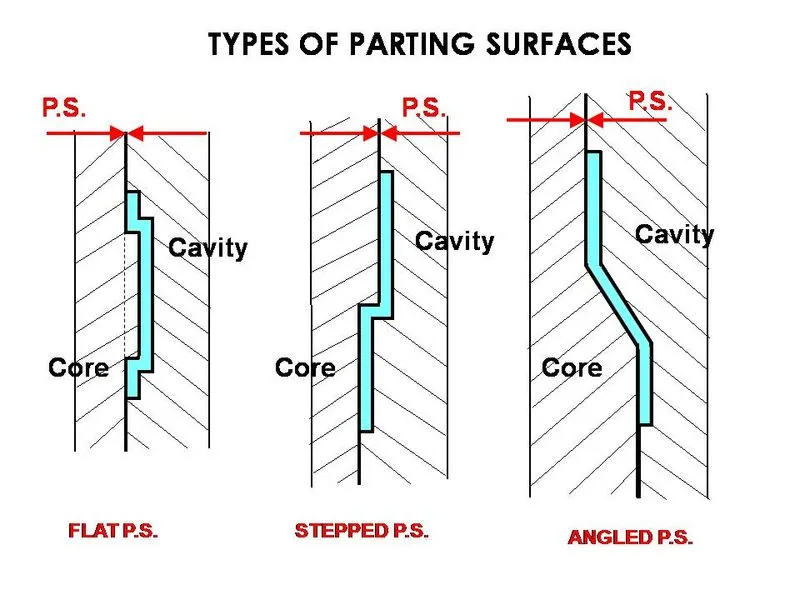
Design parting surface should follow the following principles
- Design the injection mold structure as simply as possible. Avoid or reduce side parting as much as
possible to reduce the complexity of mold making. - Ease of de-molding. As far as possible, for instance, the plastic parts should stay in the fixed half of the
injection mold and ejected by ejection system, avoid side de-molding action. - Ensure the dimensional accuracy of the molded parts. Try to make the parts with similar
dimensional accuracy requirements in the same module to reduce manufacturing and assembly - Ensure the appearance requirement of the molded parts. Flash or mismatch occurs usually on the parting
surface, so the parting surface should not be designed on any high-quality requirement surfaces. - Ensure adequate venting. If possible, the parting surface should be placed at the end of the mold flow.
Parting line
A parting line, in the industrial casting of molds, is borderline in which draft angles change direction. That is, it is the dividing line that splits the core and cavity halves of a molded part. It is sometimes a starting point for the mold parting surface.
Parting lines on injection-molded parts is a popular topic for product designers. Accordingly, this tip covers the types of parting lines you may encounter on plastic and liquid silicone rubber molded parts, and how you can properly address them.
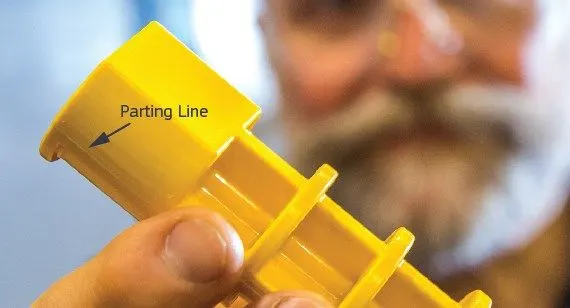
When you are developing a 3D CAD model to be molded, you may not spend much time thinking about where its parting line will be, but it's worth noting because the location can affect your part in several ways. On some parts, the location for the parting line is right down the middle, while on more complex parts, it may not be as obvious.
Take, for example, a simple plastic cup. The outer face is formed by one mold half (A-side), while the cup's inner surface and brim will be formed by the other mold half (B-side). The parting line occurs along the outside edge of the brim of the cup. For other designs, parting lines vary with geometry. A molded yellow flower, used as an art piece for children, depicts a parting line along its outer petals.
Complex Shapes Present Challenges
When a design is a complex shape, determining where the parting line will be located can be more complicated. You can assume that if you send an undrafted 3D CAD model of such a part, Protolabs will determine where the parting line should be. However, in designing such a part, you might want to think about the parting line for one simple reason: Designers and molders look at parts differently. Molders share your interest in producing the best possible part, but the focus is on molding it correctly, whereas designers focus on how it will function after it comes out of the mold. The location of the parting line can affect both.
First of all, the location of the parting line determines the direction of the mold opening and, consequently, the direction in which features must be drafted for easy ejection. Second, it affects where any vestiges left by the mating surfaces of the mold halves will be, and potentially, how those vestiges will look. Third, parting line location can also impact the cost of mold making and the type and cost of secondary operations needed to finish the part.
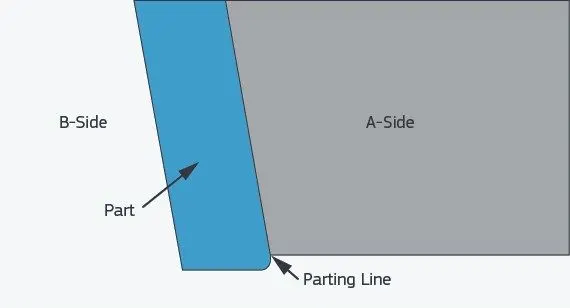
The plastic toy soldier is an obvious example of a design with a challenging parting line, but the issue can come up on simpler parts as well. For example, a straightforward geometric design with radiused or rounded edges can also be problematic. The parting line has to trace the path along which a tangent to the surface is parallel to the direction of the mold opening. In Figure 2, the parting line has been placed across an otherwise smooth surface. Any mismatch in mold edges will create a fairly obvious seam, so a parting line in this location would create a need for tighter tolerances and potentially increase milling costs. The increased likelihood of flash could also impact both the cosmetics and functionality of the part, potentially making the assembly of finished parts more difficult. If the parting line is instead placed along a sharp edge, the seam would be camouflaged, and the undesired manufacturing, functionality, and cosmetics issues outlined above (see Figure 3) would be avoided.
Liquid Silicone Rubber Parts
Designing parts for liquid silicone rubber (LSR) molding is similar to thermoplastic molding, though with the LSR processes, additional preparation to prevent flash should be considered. LSR flows into the mold as a liquid and will fill into gaps as small as 0.0002 in., which can result in a flash. Though parting lines on LSR parts are likely less visible, and less intrusive, they are harder to prevent. You should also make sure that parting lines on LSR are not on a sealing surface. Simplifying and minimizing parting lines on LSR parts will help you get cleaner parts as quickly as possible.
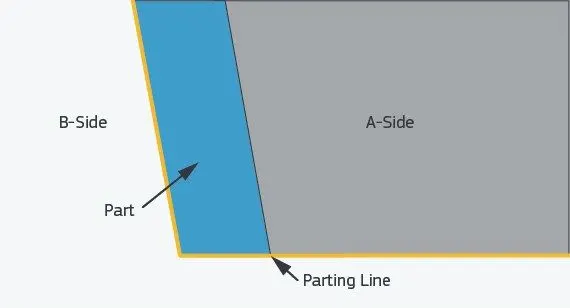
Being Aware of Parting Lines
There are several ways to address parting line challenges with all injection-molded parts. An awareness of the significance of the parting line is a good start. As stated earlier, parting line location is obvious and not a problem on many parts. For more complex parts, you may be able to use tools within some CAD packages to locate and evaluate split lines, or you can just upload a 3D CAD model online and we'll propose a parting line and suggest an appropriate draft based on that orientation. Our software may also point out that the part cannot be made in a straight-pull mold and that design changes, side-actions, and/or pickets may be required.
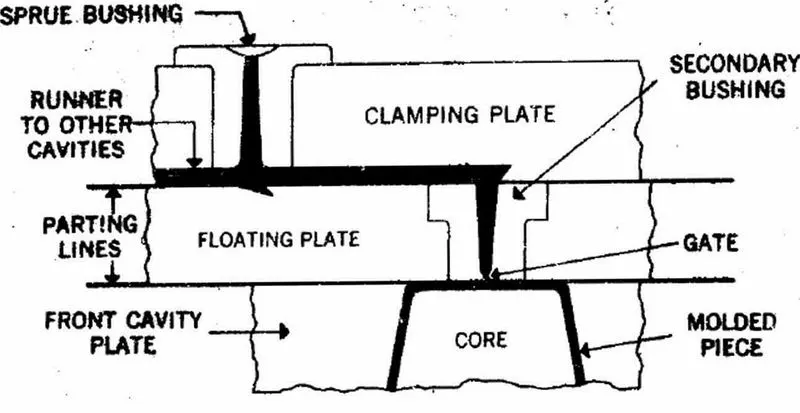
Advantages of parting line:
The parting line of casting needs to be determined early in the design process. When determining the location of the parting line the part designer and die-cast engineer should work together to consider part functionality and die casting process. Often it is useful to have most of the geometry in the ejector half; as this prevents the casting from sticking in the cover half.
The parting line is created where the two halves of the die meet. Gates overflow and vents will connect to the casting at the parting line. Also, a flash will form at the parting line when the pressure from the injected metal tries to force the die halves apart. During the trimming process the gates, overflows, vents, and flash will need to be removed by the trim die. A well-designed parting line will ease the trimming process.
When flash occurs, it increases the thickness of the parting line; altering dimensions measured across the parting line. For critical dimension, it is important to have measurements in only one die half to reduce dimensional tolerance.
The parting line can also affect the life of the die. Metal injected straight onto a surface will erode that surface faster. Positioning the parting line to allow the metal to flow more smoothly will improve die life and casting quality. Cosmetic surfaces are typically placed on the cover side of the casting.
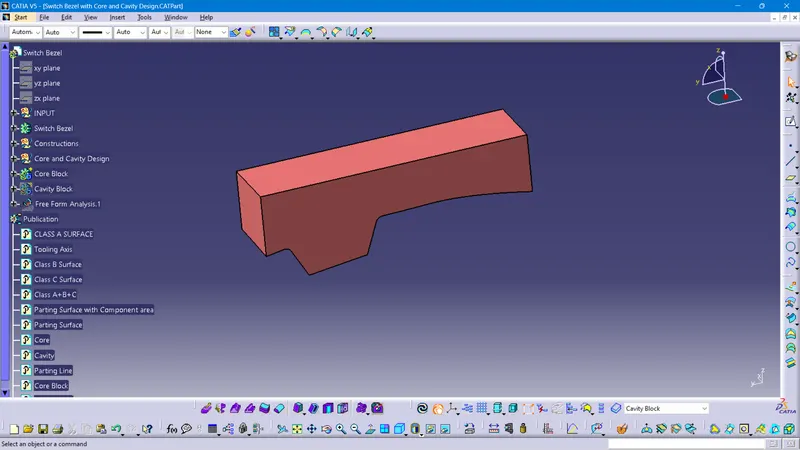
Core Block
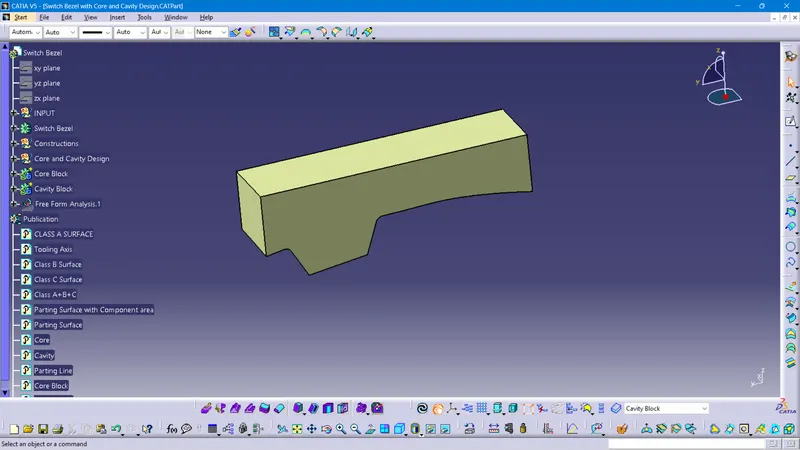
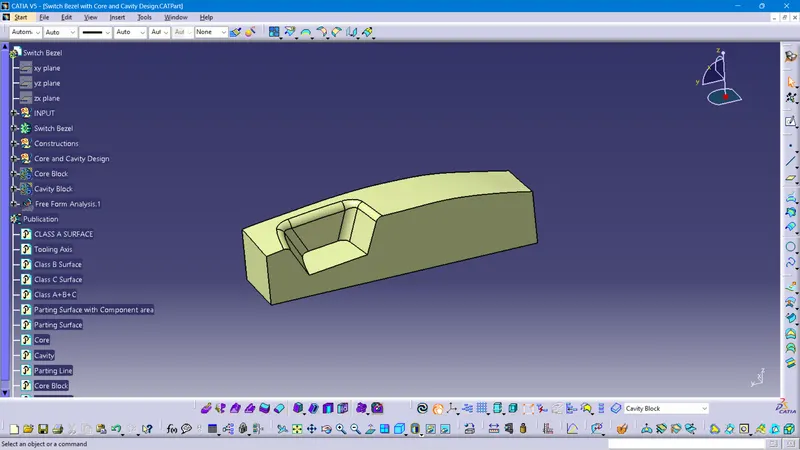
Cavity Block
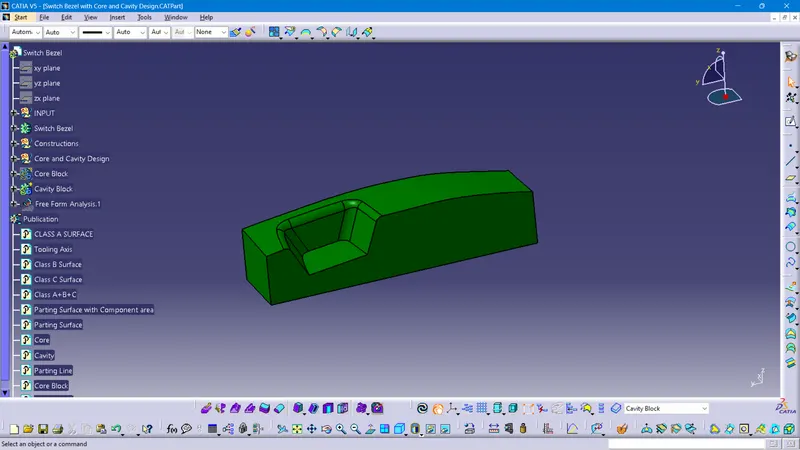
Parting Surface with Component Area
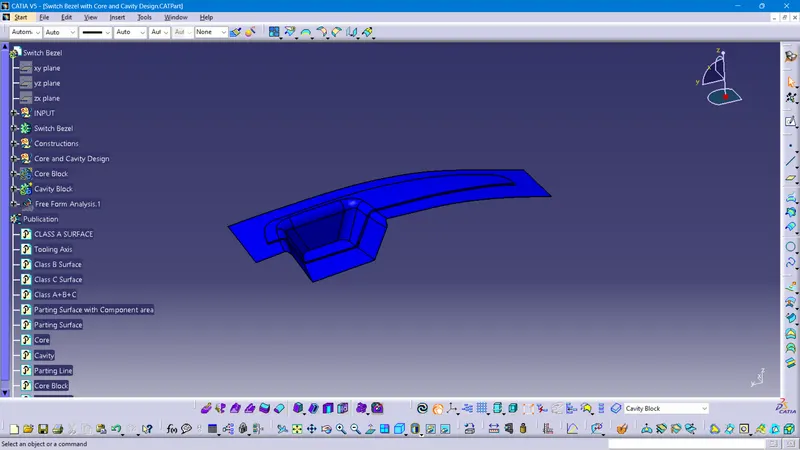
Parting Surface
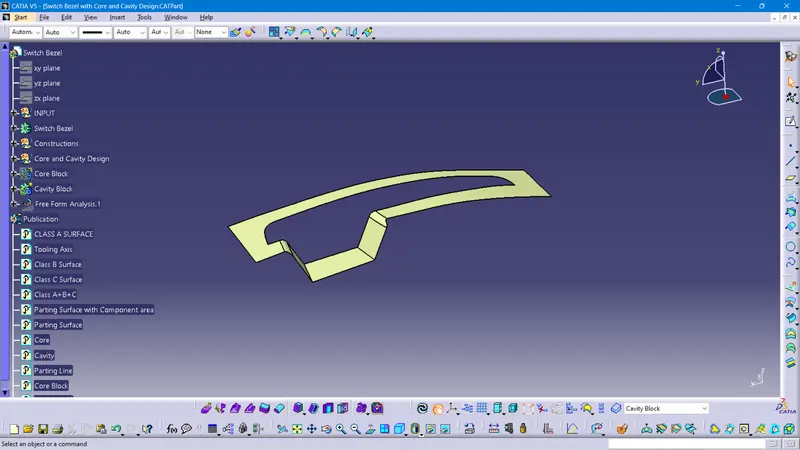
Parting Line
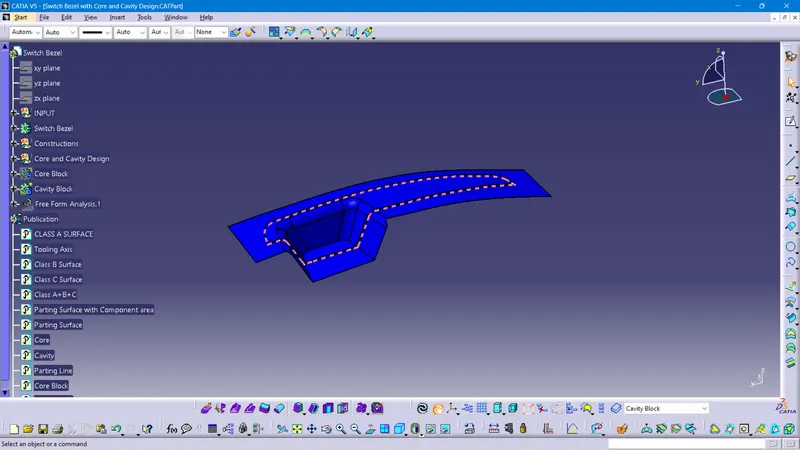
Views of the parts
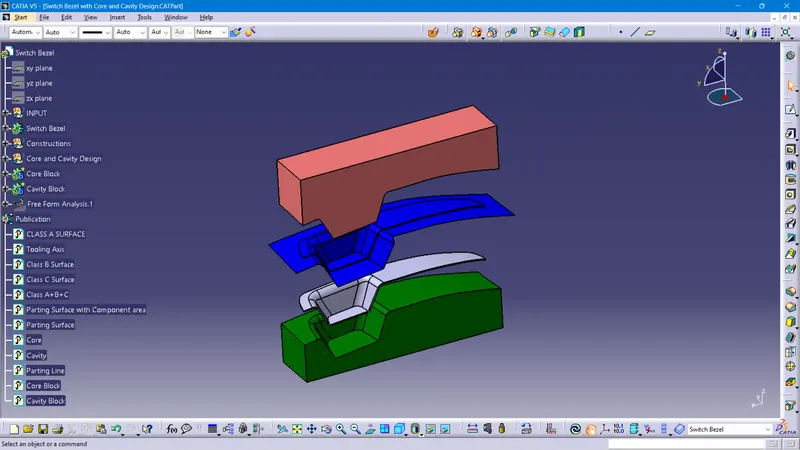
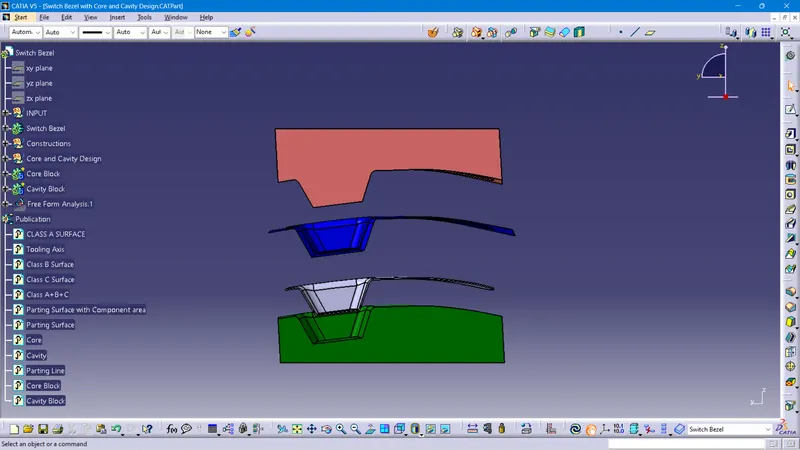
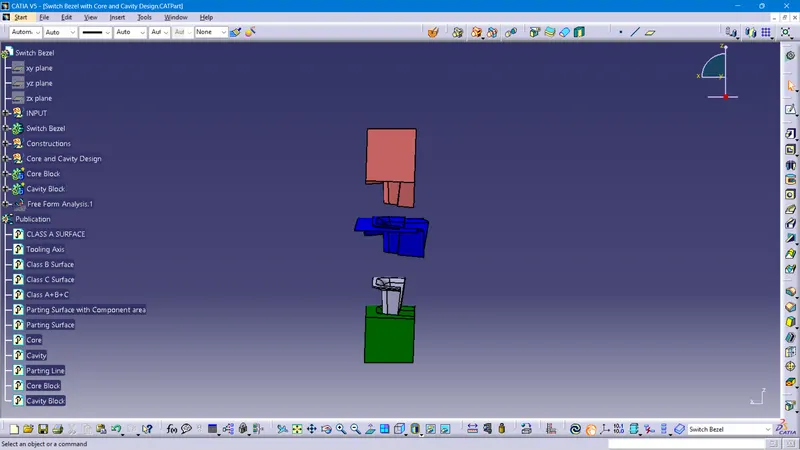
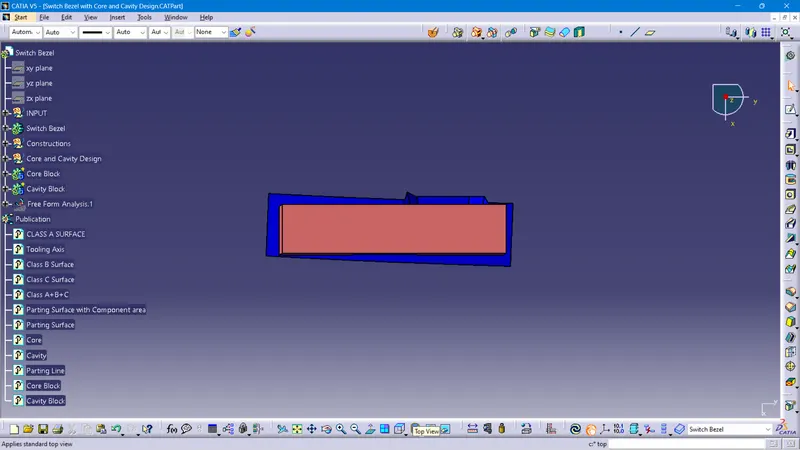
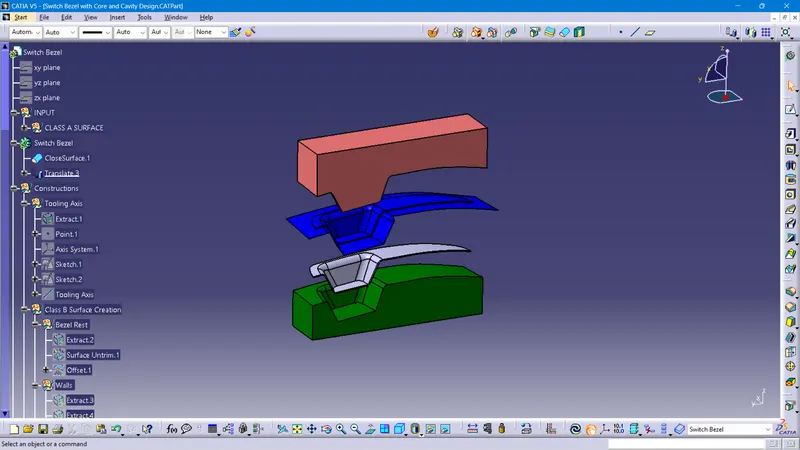
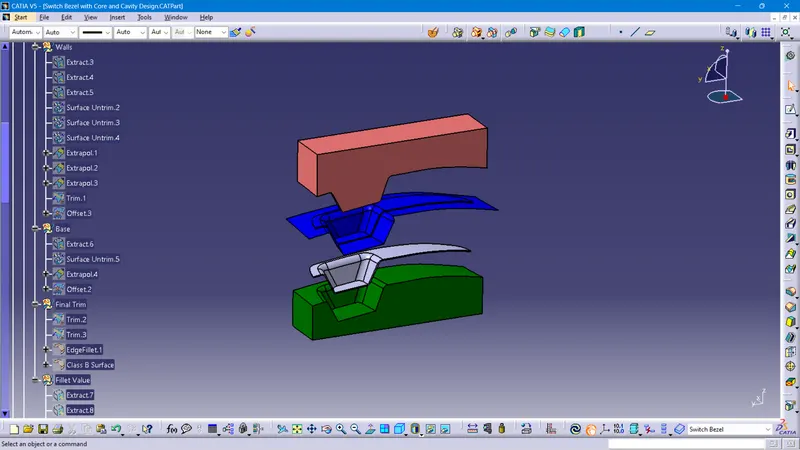
Feature Tree of the parts
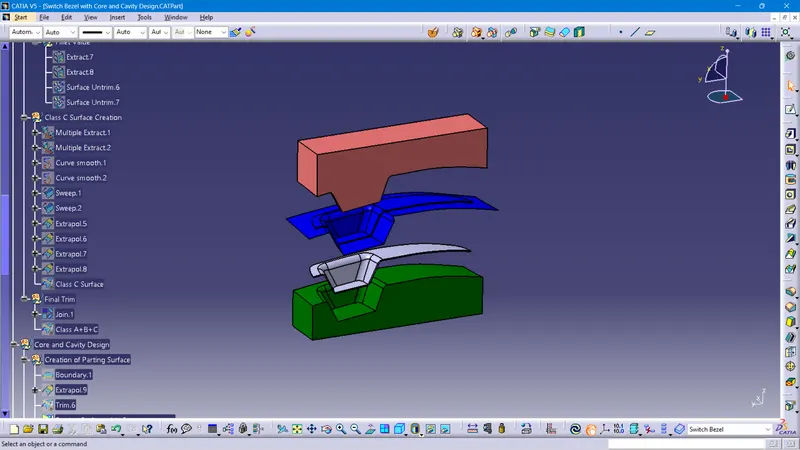
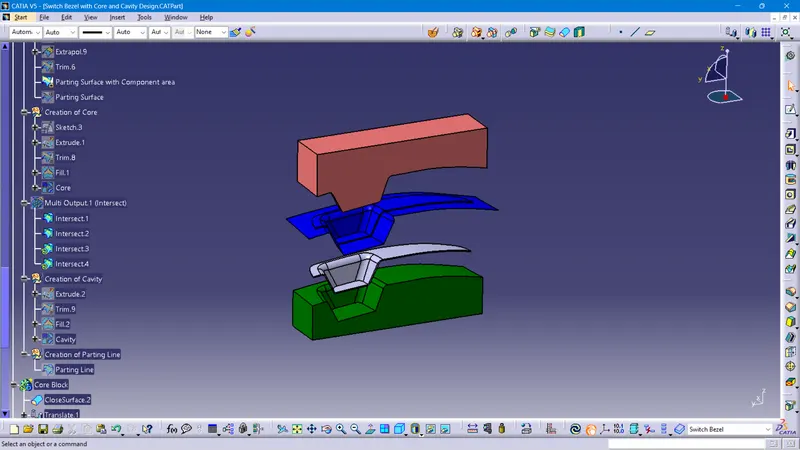
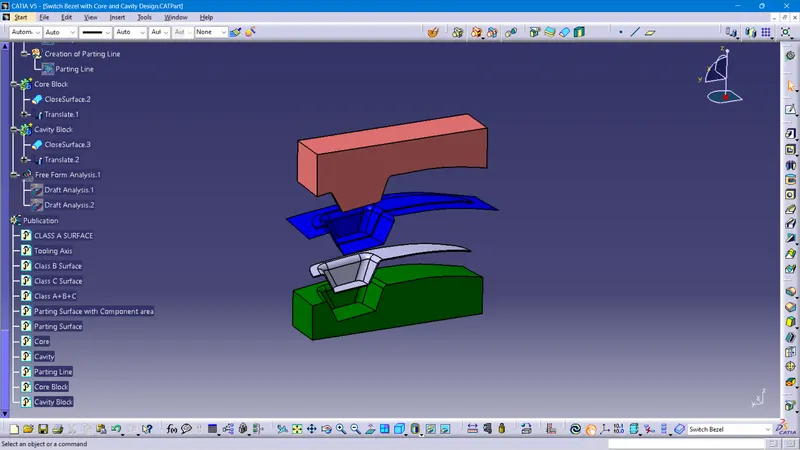
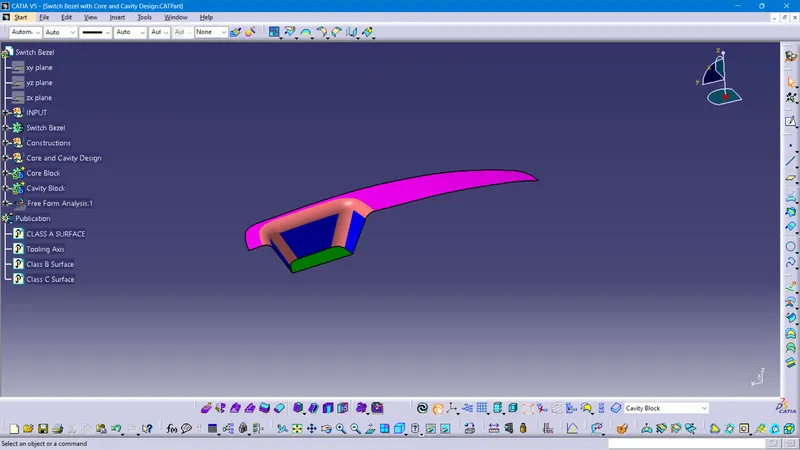
Performed draft analysis closed surface.
The green color indicates drafted walls above 3 deg.
The red color indicates drafted walls from 0-3 deg.
Blue color indicates negative deg.
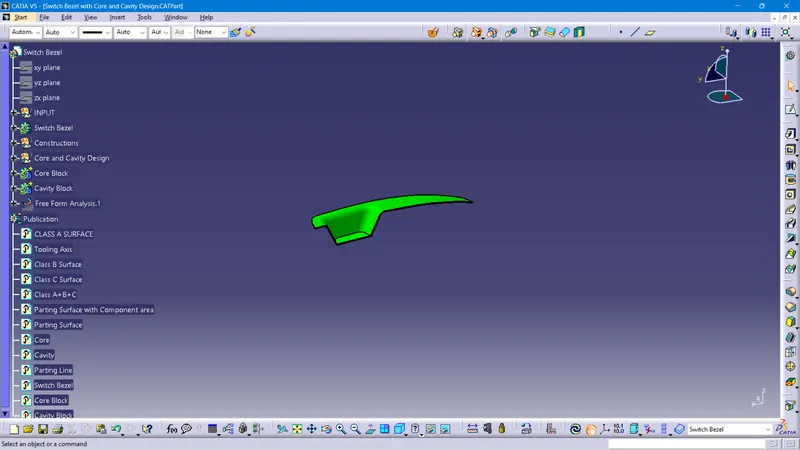
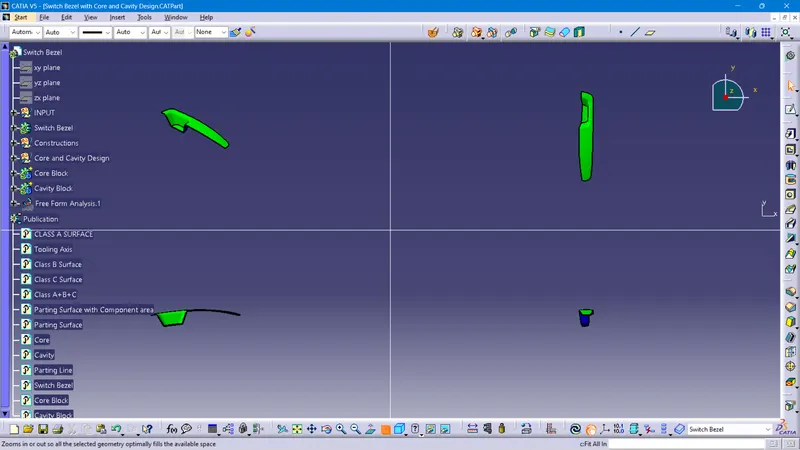
Analysis shows the drafted walls of the switch bezel are above 3 degrees which is permissible for manufacturing in injection molding
Conclusion
The Design of the Core and Cavity for the Mold of the Automotive Plastic Component – Door Switch Bezel is completed using concepts of Parting Surface, Parting Line, Draft angle, Draft Analysis for Class A and Final enclosed surface, Tooling Axis creation, and implementation, Class B and Class C creation and conversion to a solid part maintaining the part thickness at 2.5mm.