Week 8 - Challenge 6 - Core & Cavity Design
Core and Cavity Design for switch bezel
Aim :
To create the core and cavity blocks for the switch bezel we have already designed as the solid part.
Objective :
- Create the required Tooling axis by using the bisecting method.
- Perform the Draft analysis on the solid model.
- Create the parting line and parting surface.
- And create the core and cavity blocks for the switch bezel.
Theory :
Tooling Axis :
Class-A surface is first analyzed to create the tooling axis or tooling direction that molds pull apart in injection molding. Tooling direction is important for plastic product design as it decides direction for mold seperation.
Steps followed for creation of tooling axis :
- Reference point is first created on extracted surface.
- New axis system is deployed to plot clearance lines.
- The X-direction and Y-direction along the class-A were used to create tooling axis.
- Graphic properties of tooling axis were change before publishing.
Draft Analysis :
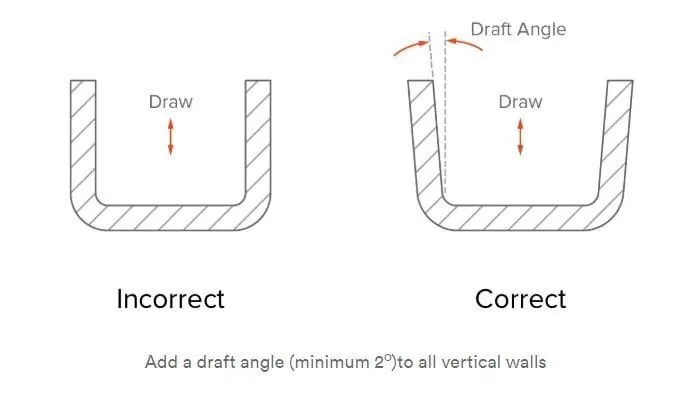
The Draft angle is the amount of taper for molded or cast parts perpendicular to the parting line. It can be measured in degrees. A functional part for injection molding has to have drafts facing both cavity and core sides to reduce the risk of damage to the parts and ensure ejection. And also important is to overcome the vaccume forces by letting air in between the metal or the plastic for the part to release properly. Adding maintaining a decent cosmetic finish.
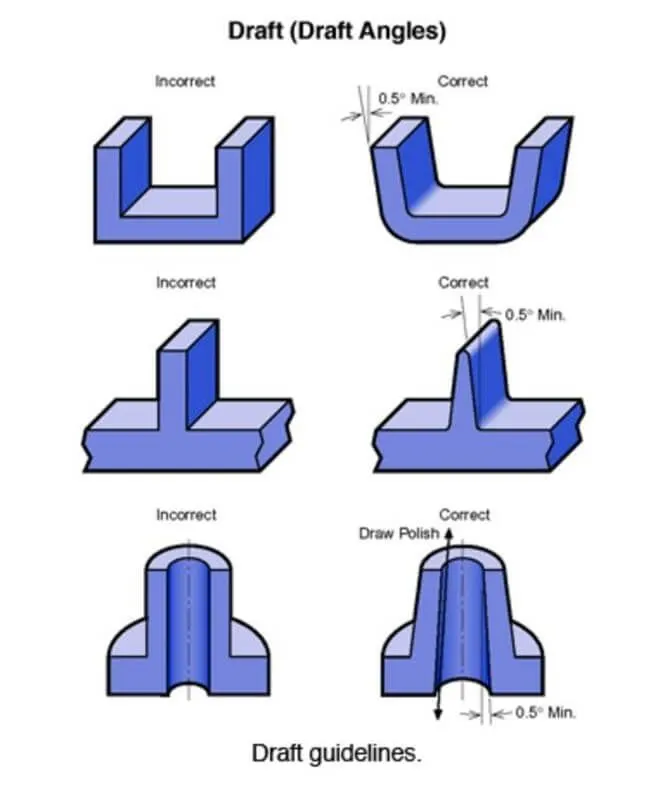
Draft should be a part of design for manufacturing and plastic product Designer should be aware of its need at the outset of the design process. This allows considerations for design requirement to be taken into account.
Nominal values for Draft angle :
- 3 Degrees is the nominal Draft angle.
- 7 Degrees for textured surface.
- At the minimum of 0.5 Degrees can be manufactured by special tools. But it will increase the manufacturing cost.
Tooling axis creation :
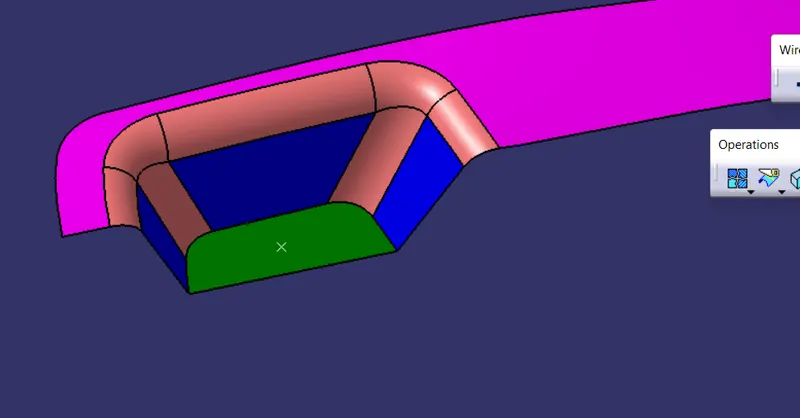
First step is to observe the given class-A surface deeply and we can say the larger flat area which is perpendicular to the Tooling axis. so by cosidering this things for this class-A surface tooling direction is near to the Z-axis. so we create the point on the flat surface as shown in figure.
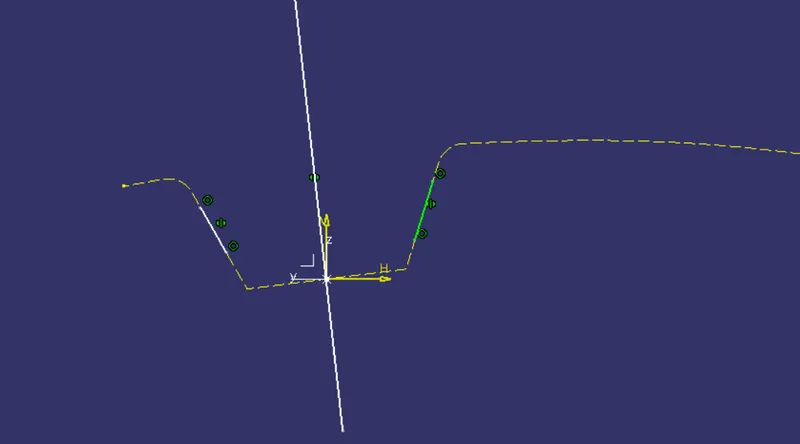
Next step is to create the reference axis from X-axis and Y-axis. so for that we take the two side flat surface as the reference and create lines along the faces in the Y-direction by using the intersecting line and by using the bisect line tool the reference axis from Y-direction is created as shown in figure.
Next step is to crate the reference axis from X-axis too. Similarly from the X-direction reference is also got as shown in figure.
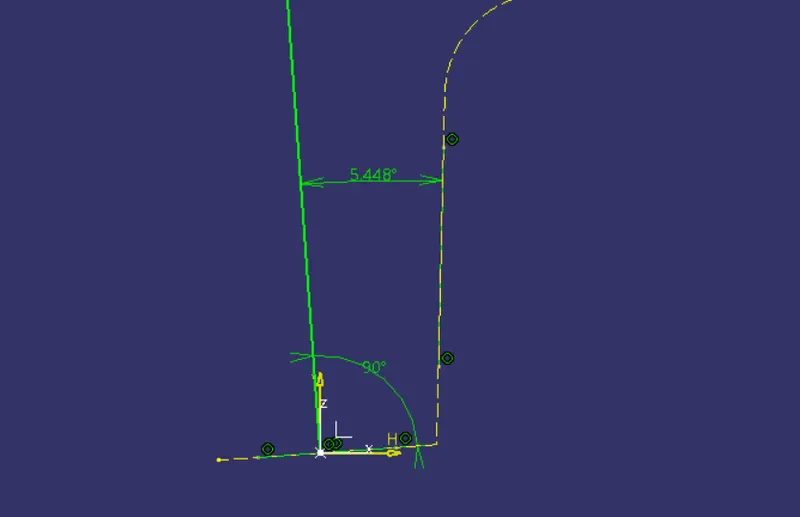
So now we got both direction reference lines so next is to create the main tooling axis. For that we create the surface along the both reference lines as shown in figure.
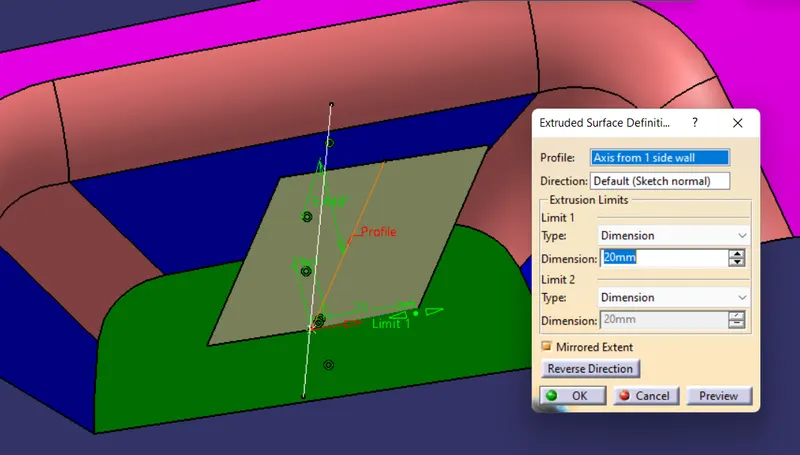
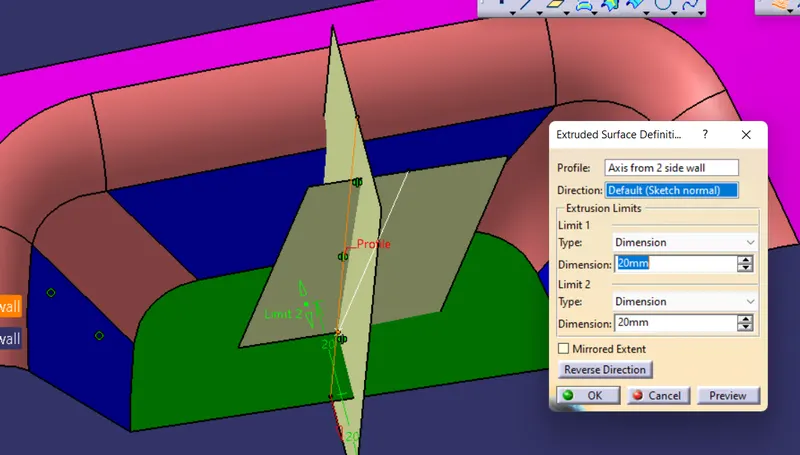
And next is using the intersection definition we got the main tooling axis as shown in figure.
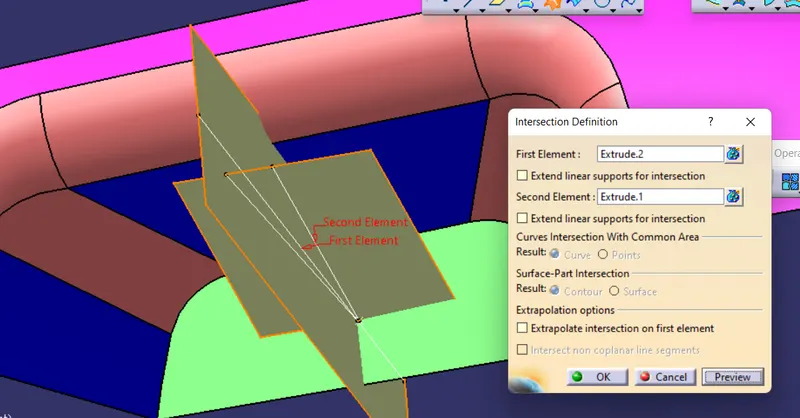
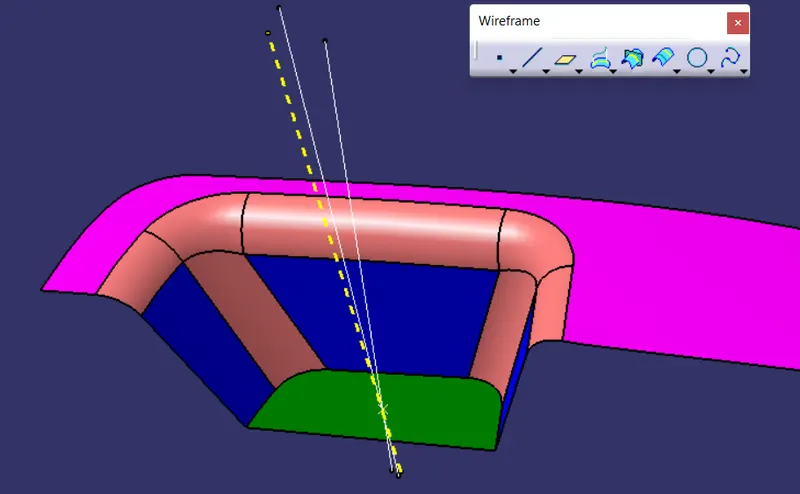
And finaly give the proper color and line type for that axis to visible clearly and publish the tooling axis.
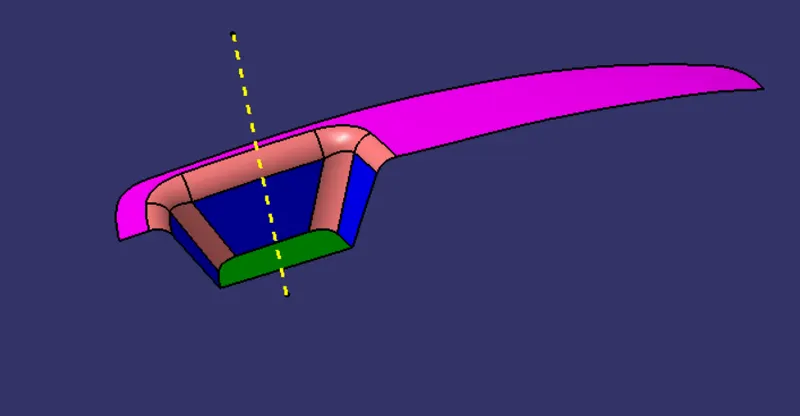
Steps followed for Draft Analysis :
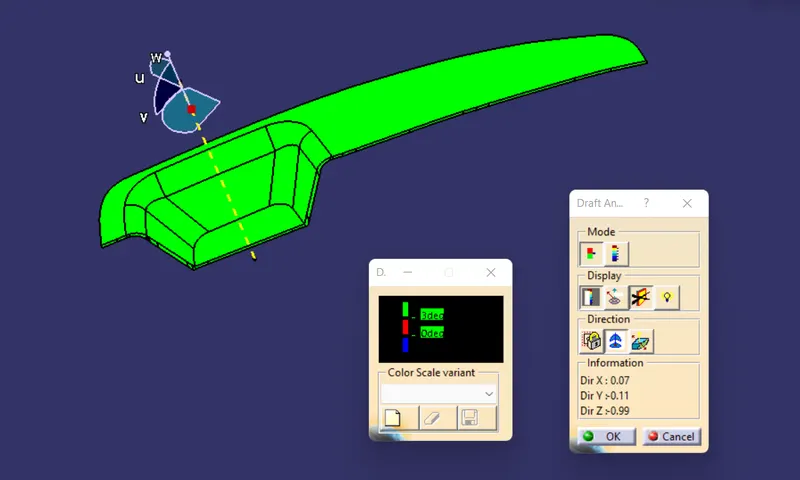
- The part created has to be changed to material mode in display frame.
- Compass is enabled and align it along with the tooling direction.
- Lock command is then applied to fix compass along with tooling axis.
- Color codes are classified and draft angle is applied.
- Running point analysis is used to display permissible draft angle.
Draft analysis for solid body :
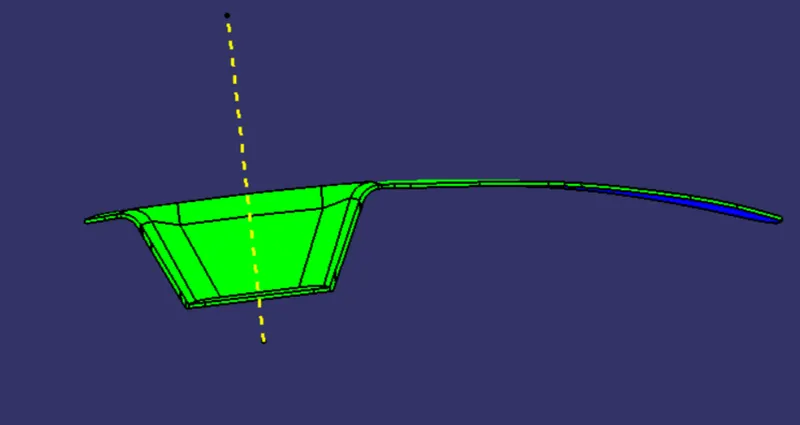
Different views :
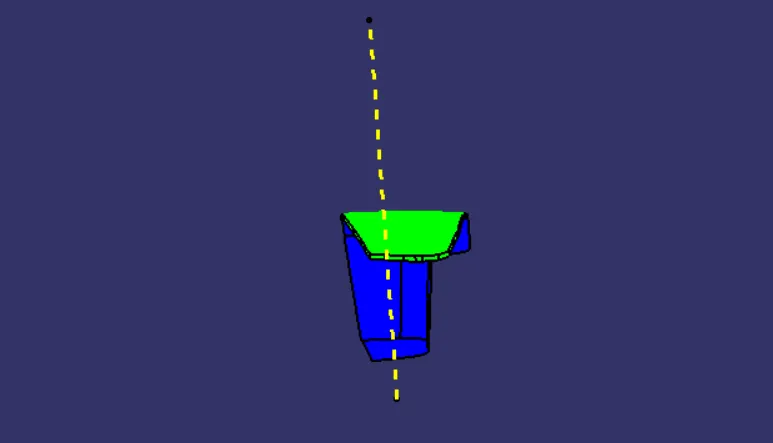
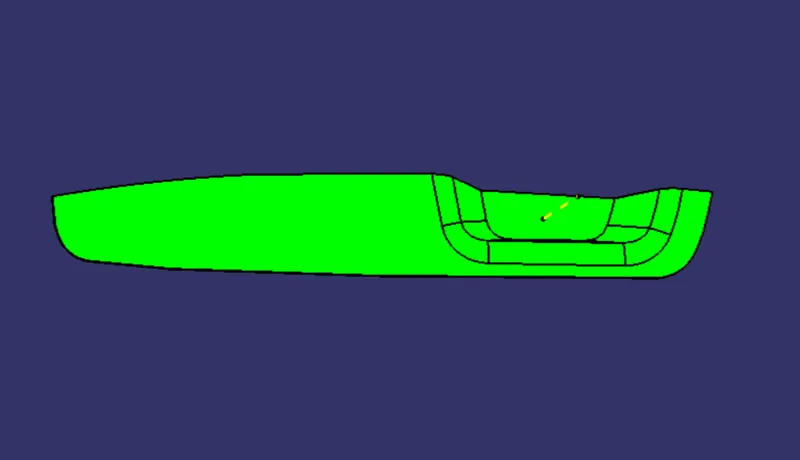
Core and cavity :
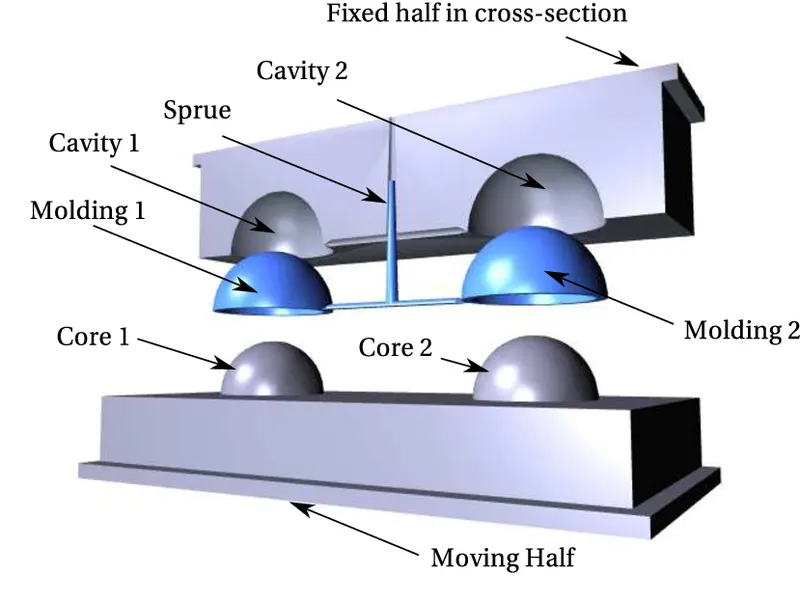
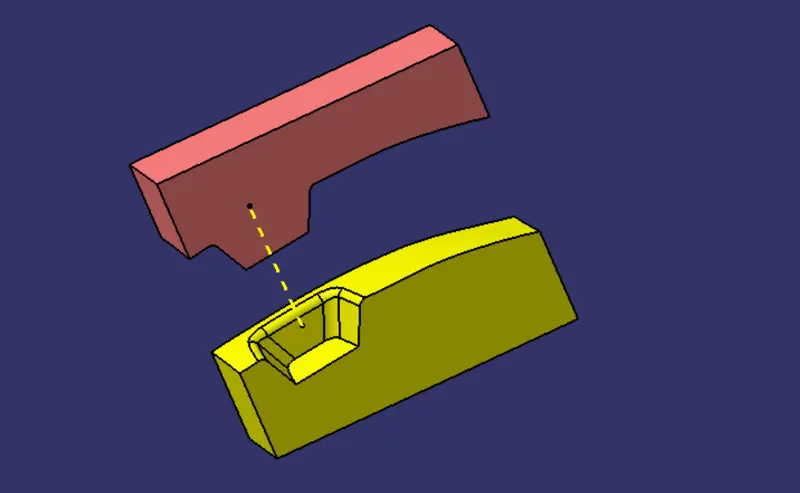
A core is the one part of the mold and it is responsible for half of the molded part. Actually core is the projection of the body and cavity is the depression of the body. These core and cavity combines to form a mold. Then the plastic material injected into these mold to get a plastic part.
Parting surface :
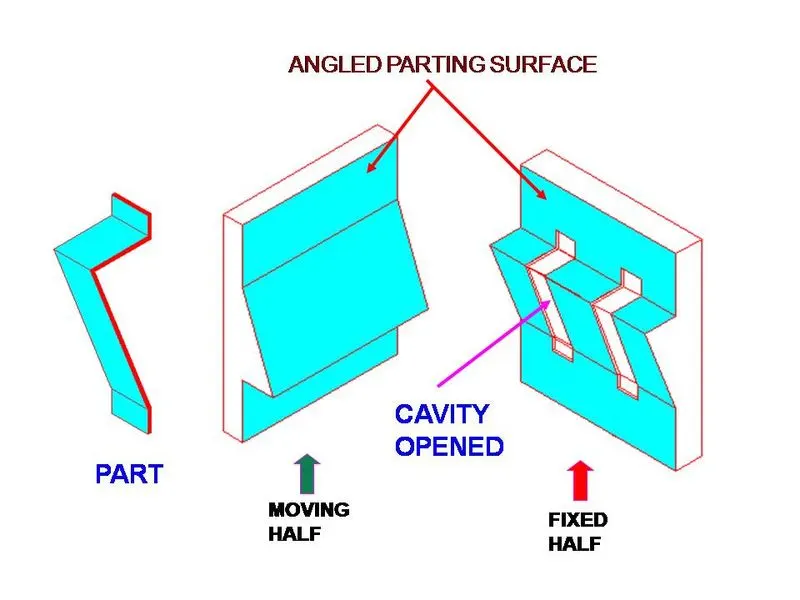
Generally injection mold has two major components the movable halve and the fixed halve, during injection molding process, these two halves are pressed tightly and form a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface are called parting surface, usually parting surface are the biggest projection outline of the part.
Parting line :
It is the area in which parting surface and component meets or it is a junction between core and cavity.
Creating parting surface :
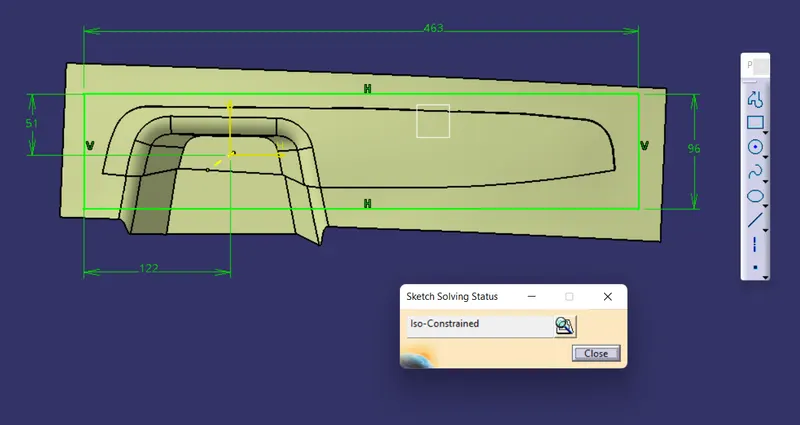
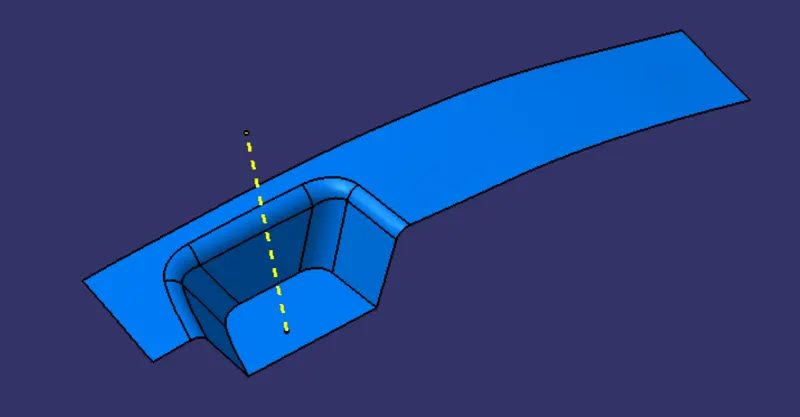
To create the parting surface we already have the untrimed part of the class B surface. And on that surface create the one rectangle for create the parting surface as shown in figure.
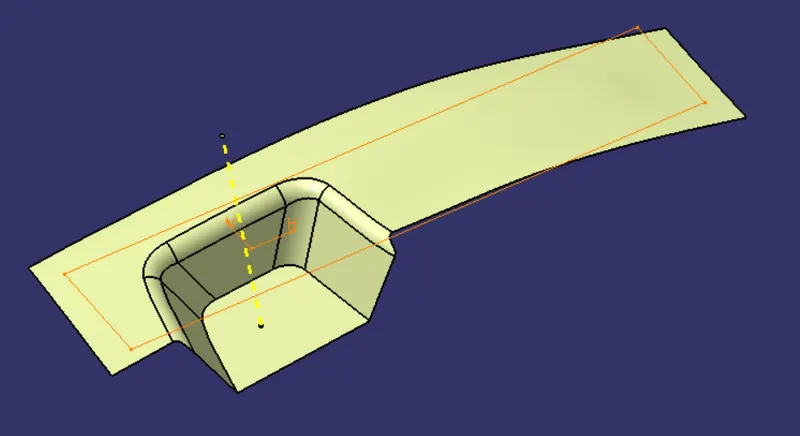
Now using the sweep tool and direction as the tooling direction create the sweep surface as shown in figure.
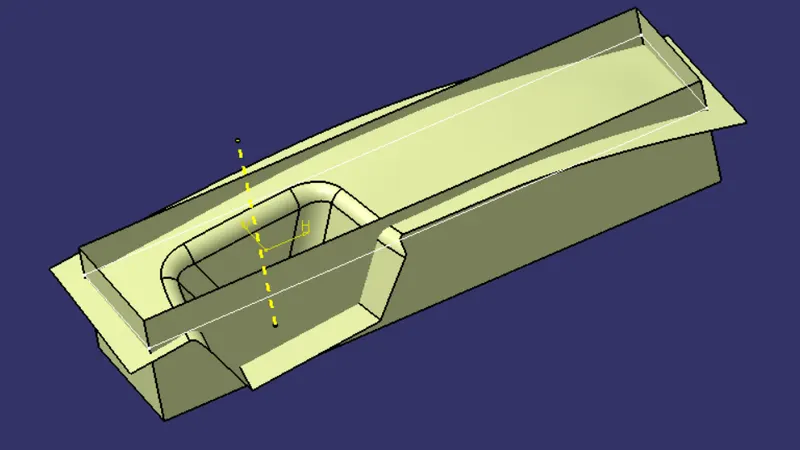
Now split the untrim part of B surface with the sweep surface we created as shown in figure.
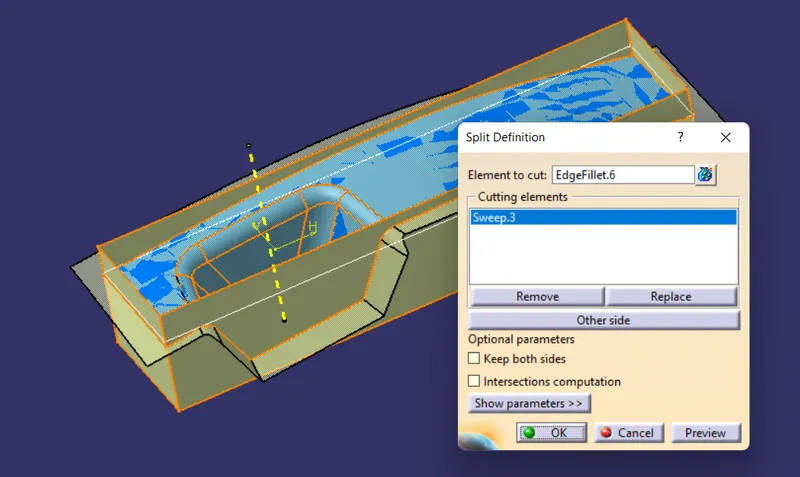
So this is the parting surface from the cavity side as shown in figure.
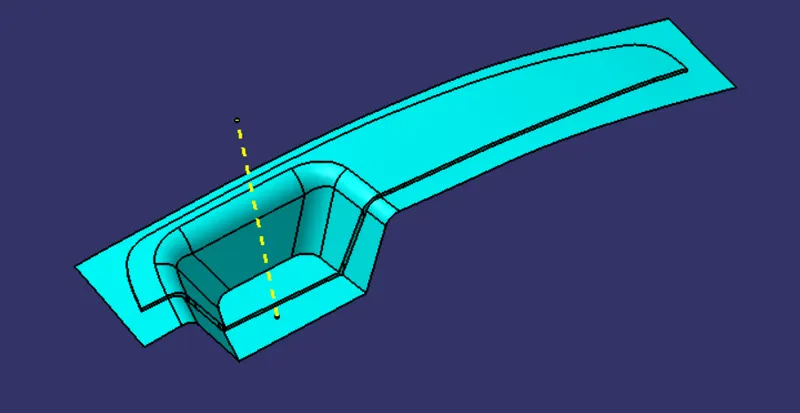
Similarly for the core side we first join the class-A with class-c and cut the inside of the untrim of class-B surface and do the same sweep and cut operation we got this parting surface from core side as shown in figure.
Creating core and cavity :
For creating the core side we take the parting surface and the rectangle created as shown in figure. And sweep the rectangle with the reference of tooling axis as shown in figure.
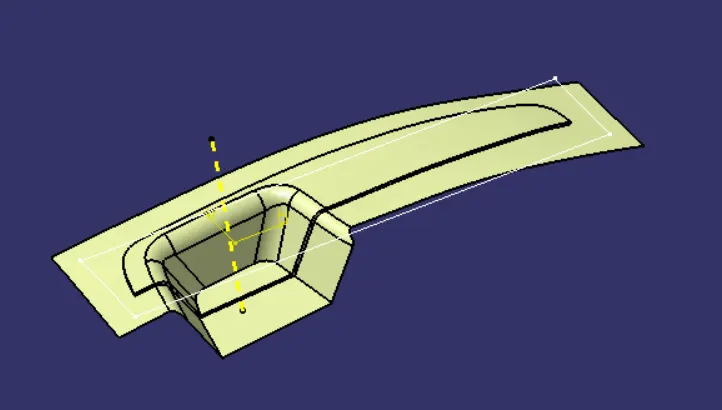
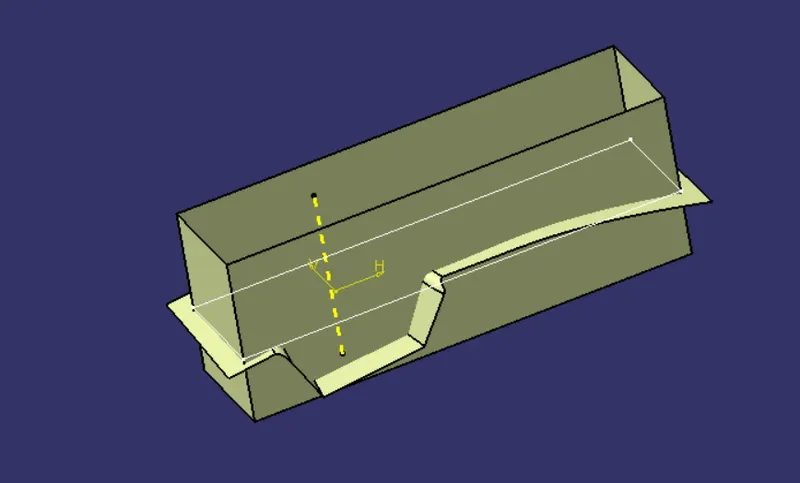
Now trim the outer sides of the both surfaces as shown in figure.
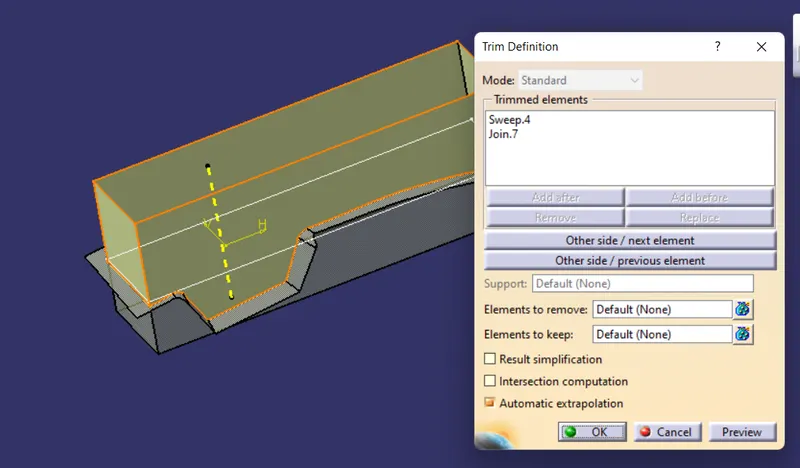
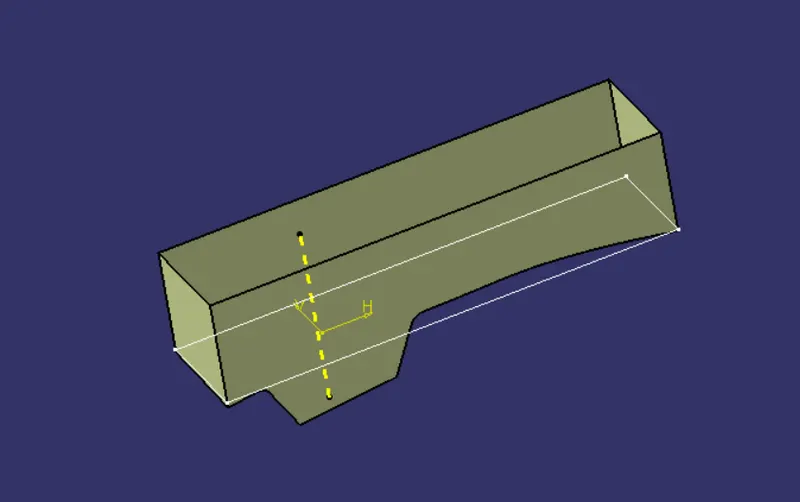
And using fill tool close the top of the surface and now it is the closed surface we can make solid by this surfaces as shown in figure.
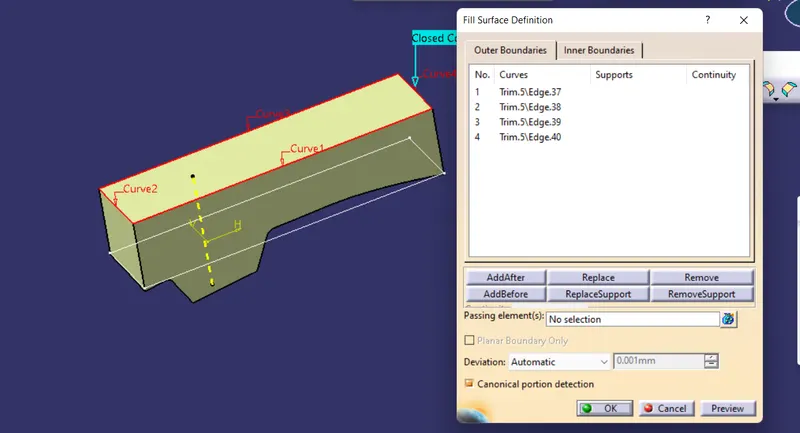
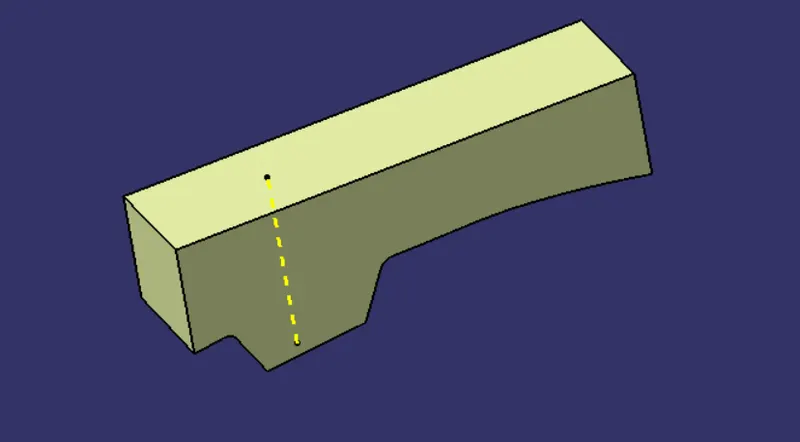
Finaly using the close surface tool this solid body of the core is created as shown in figure.
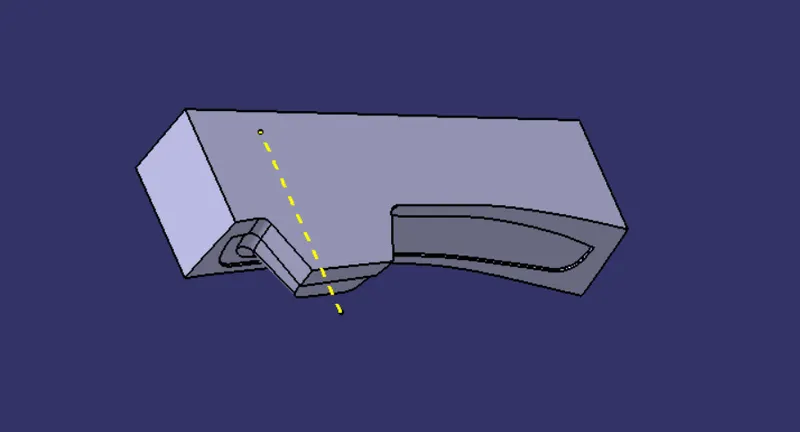
Similarly this cavity solid part is also created usning the class B surface impression on it as shown in figure.
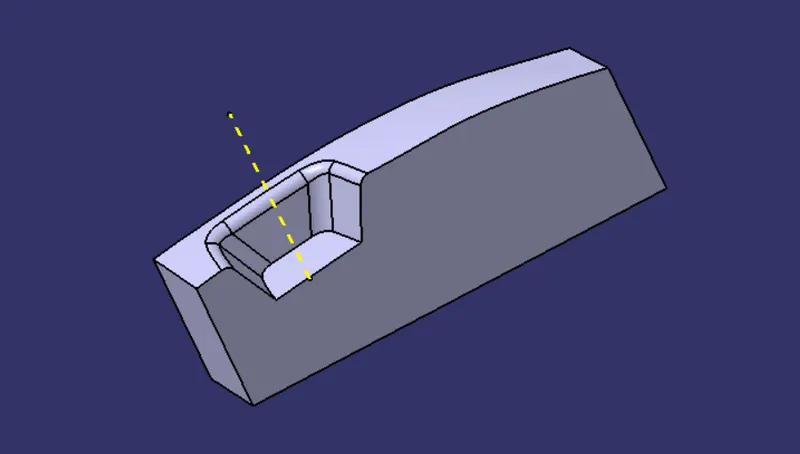
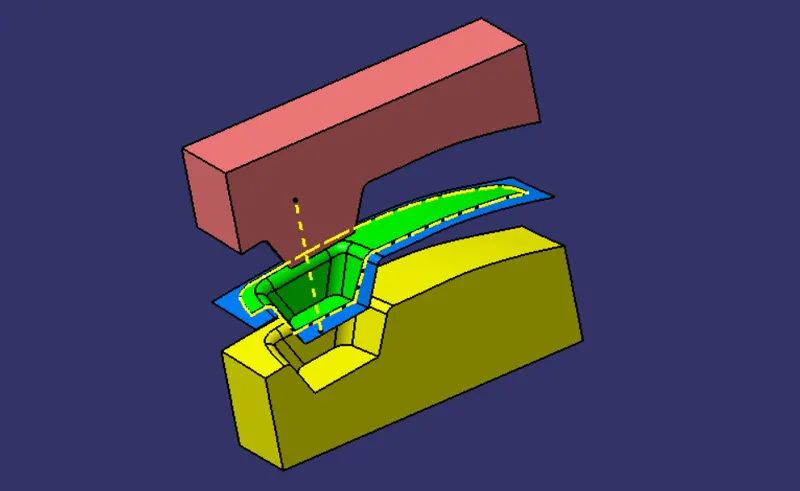
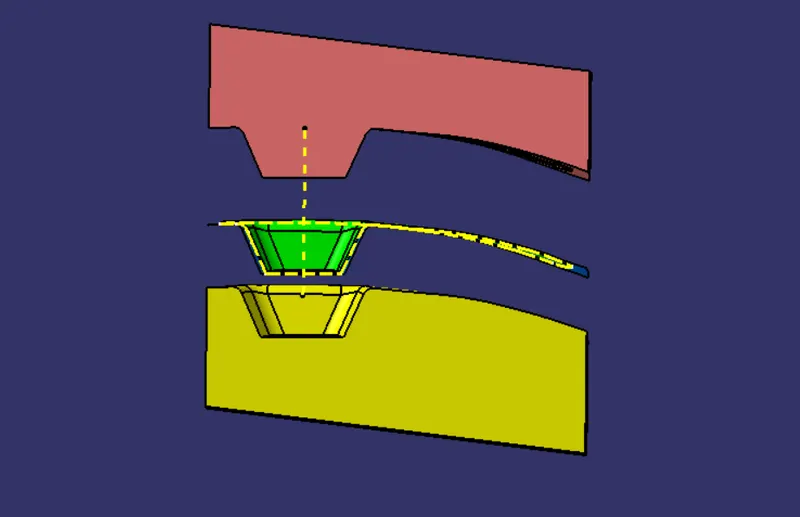
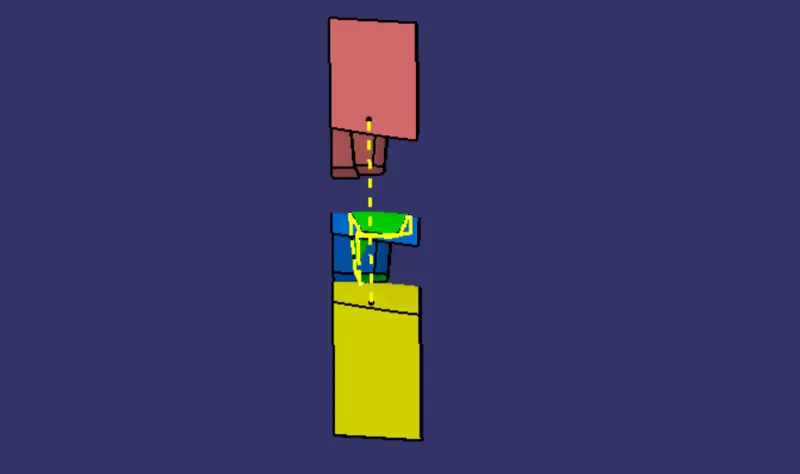
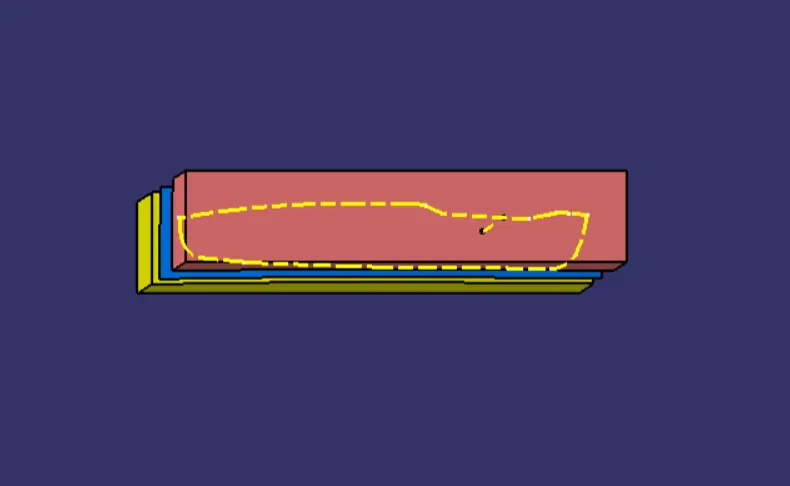
Core and cavity :
Parting surface : Blue color surface
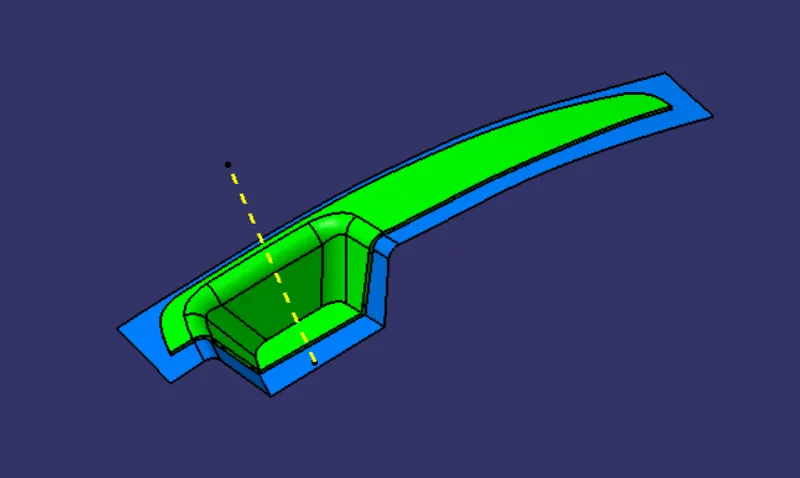
Parting line : Yellow color line
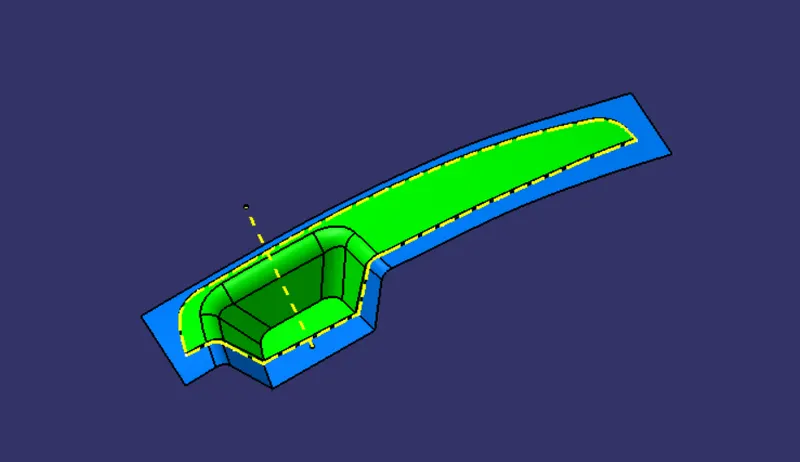
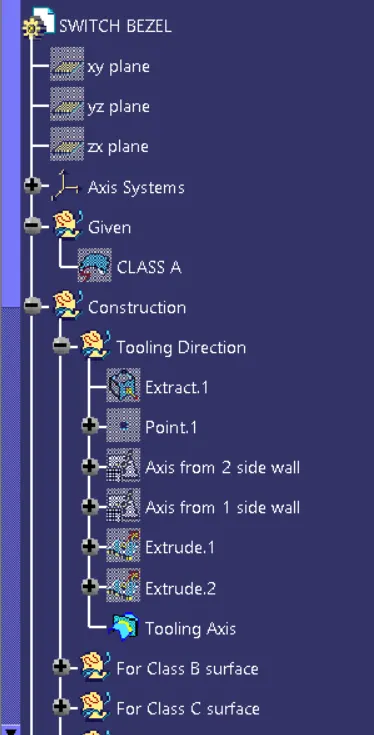
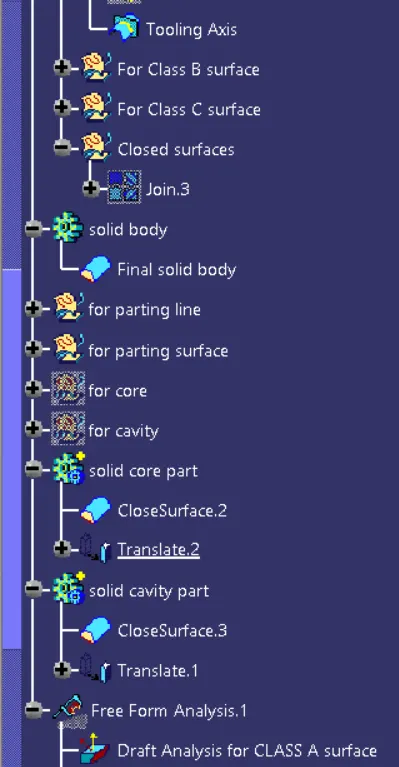
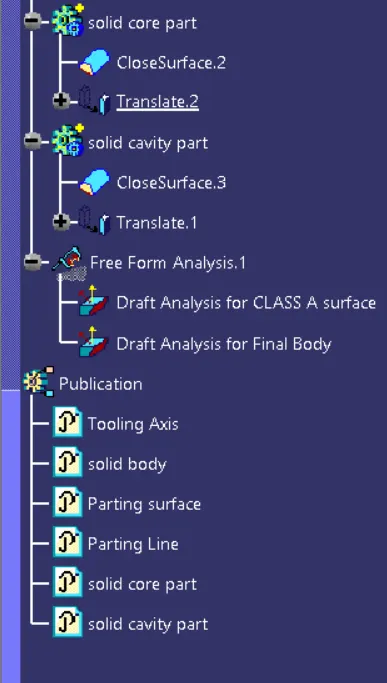
Tree structure : For creating parting surface, parting line, core and cavity.
Iso-metric view :
Front view :
Side view :
Top view :
Conclusion :
Hence the core and cavity blocks from the switch bezel we have already designed as the solid part is created sucessfully. And here we create the parting surface and the parting line. from this Draft analyis and parting surface we try to make the parting surface as flat surface as much as possible which is useful for large number of prodction the part.