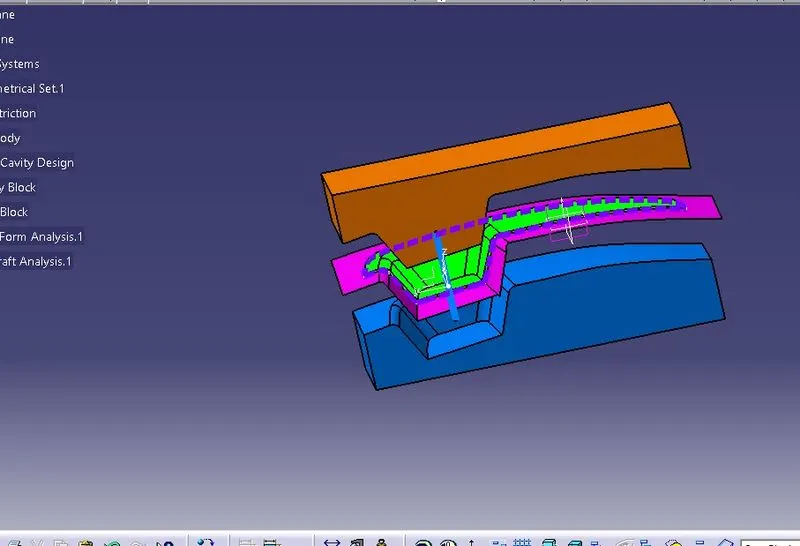
Week 8 - Challenge 6 - Core & Cavity Design
AIM:
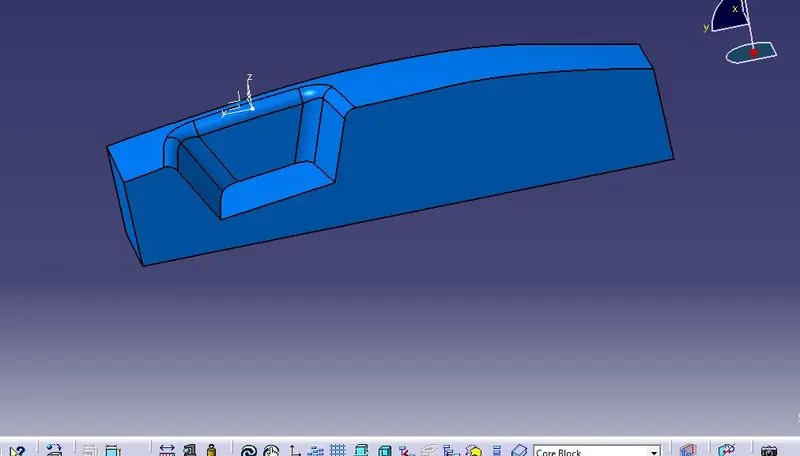
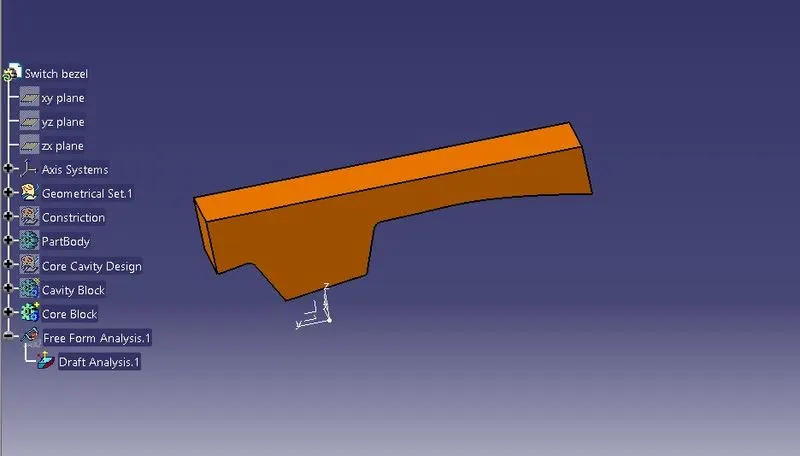
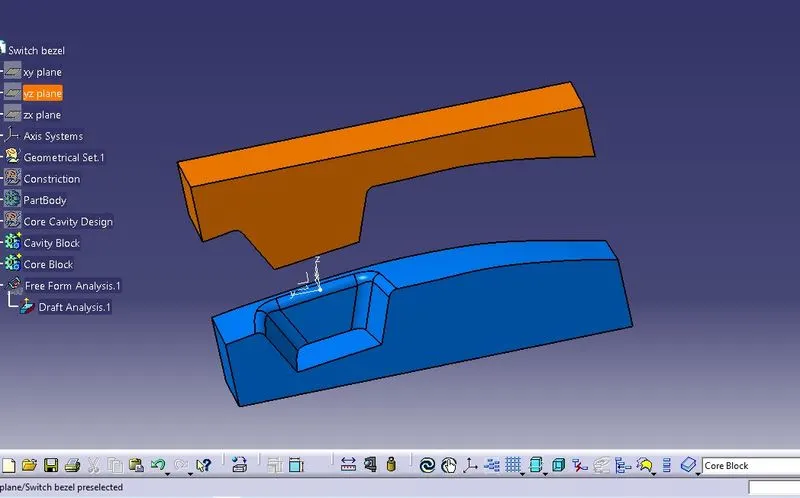
To create the core and cavity for the switch bezel considering all design rules.
TOOLING AXIS:
IT IS THE AXIS IN WHICH THE DIRECTION CORE AND CAVITY OPEN. THIS IS THE VERY IMPORTANT FOR PRODUCTION OF PLASTIC COMPONENT. MOST OF THE DEFECT WILL DONE IMPROPER TOOLING AXIS CREATION BY THE PLASTI DESIGNER.
THERE ARE SO MANY METHODS FOR CREATION OF TOOLING AXIS. INTERSECT IS THE ONE OF THE METHOD FOR CREATING THE TOOLING AXIS.
DRAFT ANALYSIS:
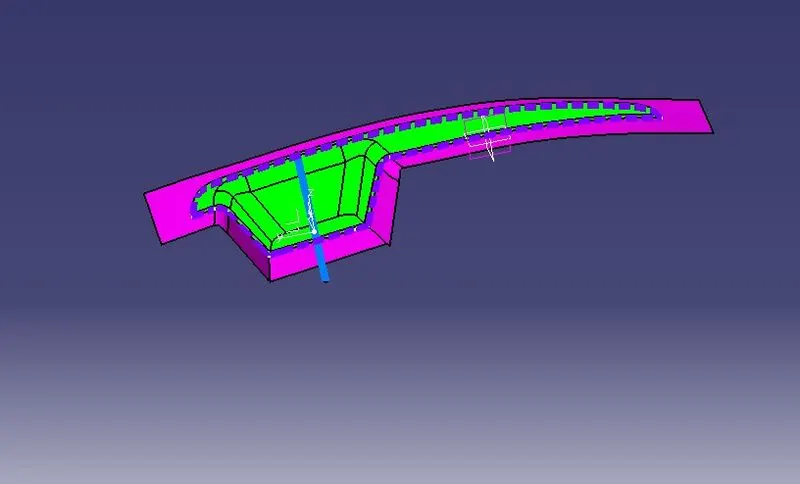
THE PURPOSE OF DRFT ANALYSIS IS TO DETECT THE PARTSHOULD BE EAISILY WITHDRAWL FROM THE CORE AND CAVITY BY USIN OF DIFFRENT COLOUR RANGES.THIS ANALYSIS WILL BE DONE BY DRAFT ANALYSIS COMMAND. FOR THIS COMMAND GO TO INSERT< ANALYSIS< FEATURE DRAFT ANALYSISTHESE ARE THE FALLOWING STEPS TO DO THE DRAFT ANALYSIS ON SWITCH BEZEL.FIRST TO CLICK THE DRAFT ANALYSIS COMMAND THE FALLOWING WINDOW WILL BE APPEARED.
CORE AND CAVITY design for switch bezel:
first of all you have full knowledge about what is, cavity, parting surface, parting line etc.
Core and cavity:
a core is the one part of the Mouland it is responsible for half of the molded part. core is the projection of the body and cavity is the depression of the body. these core and cavity combine to form a mound. then the plastic material injected into this mound to get a plastic part.
Parting Surface:
injection mold has two major components one is core and another is cavity. during the injection molding process, these two halves are pressed tightly from a sealed hollow to avoid the melt flow leakage and maintain certain holding pressure, the pressed surface are called parting surface , usually parting surface are the biggest projection outline of the part.
Parting Line:
it is the area in which parting surface and component meets or it is a junction between core and cavity
and the parting surface has some set of rules because the product quality mostly depends on the parting surface.
DESIGN PARTING SURFACE SHOULD FOLLOW THE FOLLOWING PRINCIPLES:
Design the injection mold simple as possible. Avoid or reduce side parting as much as possible to reduce complexity of the mold making.
Ease of de-molding as far as possible, for instance the plastic parts should stay in fixed halve of injection mold and should ejected by ejection system avoid, side de-molding action,
Ensure the dimension accuracy of the molded parts, try to make the parts similar dimension accuracy requirements in same mold to reduce manufacturing and assembly errors.
Ensure appearance requirement of molded parts, finish or mismatch usually occurs on parting surface, so the parting surface should not be designed on high quality requirement surfaces.
Ensure adequate venting. If possible, parting surface should be place at the end of the mold flow. This is going to be advantage of filling and venting.