Week 7:- Base Unit Design Challenges 1
Week 7:- Base Unit Design Challenges 1
1. What is the Base Unit? What are the typical parts of the Base Unit?
Base unit -
A base unit is a unit on which all other units of tools and also other parts necessary for the tool like pneumatic valve box, trunking cable path, etc are assembled.
A base plate is a machined plate that has a thickness of 25-40mm. it is made of a material like steel, or aluminum.
The base unit mounts parts like a trunking channel, base plate, valve box, measuring hole cover, eye bolt, pedestal, weld bars, and floor plate.
Holes will be drilled on the base unit to mount the parts on it.
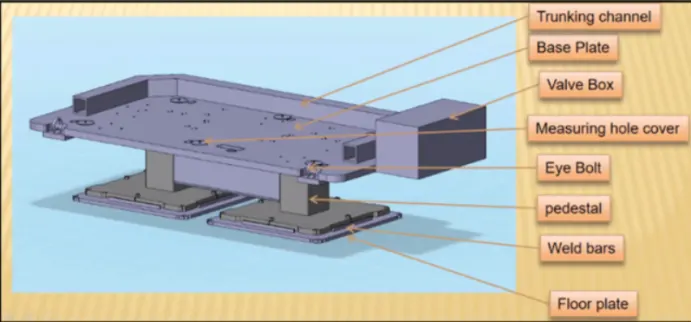
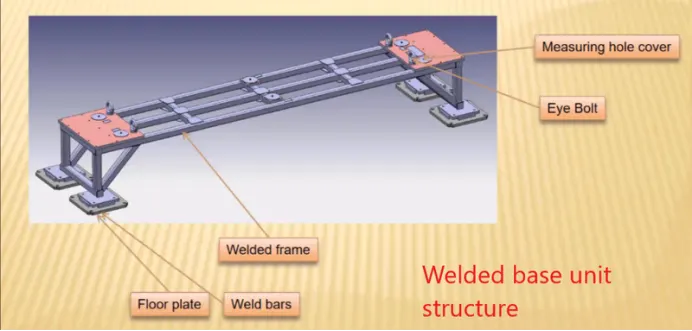
Parts of base unit -
Pedestal: -
It is used to connect the base plate with a floor plate.
The pedestal can be a standard part of a make part, depending on the size and height of the fixture.
Standard pedestals are available at different heights.
Pedestals are also available in different inclinations.
Depending on the size of the base plate, the number of a pedestal for a fixture can vary for load distribution.
Trunking channel -
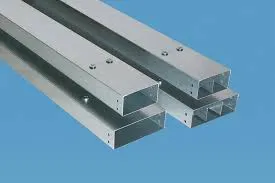
The trunking channel is a duct that accommodates all electrical and pneumatic hoses and wires for the unit of the tool.
The trunking channel is available in different thicknesses and different sizes.
VALVE BOX-
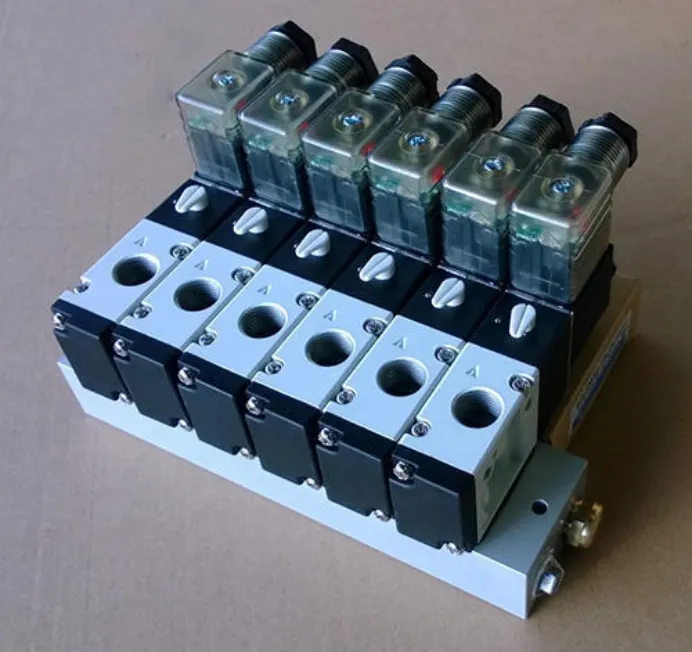
The valve box is a standard part that will accommodate all the pneumatic valves for the unit.
The valve box is the box that includes different solenoid valves.
The trunking channel includes all the pressure inlet cables going to pneumatic parts of the fixture & protects them from damage while the operation is in process.
EYE BOLT -
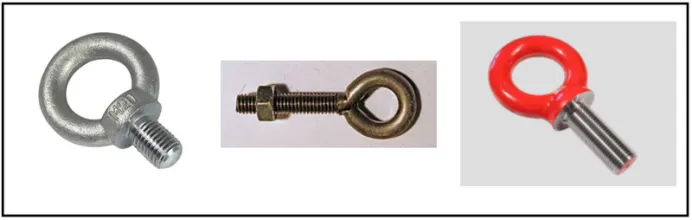
Eye bolts are the bolts that are used to lift fixtures for transportation by inserting hooks into them.
For example, usually we use M20 bolts that are bolted on the base plate.
Used for transportation purposes, sometimes forklift holes will be provided.
FLOOR PLATE -
The floor plate is grounded to the floor with a fixed bolt on the ground.
Floor plates are also called foundation plates.
There will be a clearance of 10mm maintained between the pedestal base plate and the floor plate.
This clearance will be used by the leveling screw, for leveling the entire tool.
Weld bars are used to weld the positions permanently after leveling is done.
A weld bar is a plate along the sides of the base plate of the pedestal.
2. What are the points need to account for while designing a Base unit?
The following are the points that are needed to be taken into consideration -
- a) The working height of the base unit is an important consideration, it depends upon the type of welding operation like manual welding or robotic welding. for manual welding fixtures, the working height should be 850-1100 mm, this may vary in different regions.
- b) The dimension and the specification of the base plate are also important to factor .below are the fundamentals given for the base plate.
Fundamental of base plate -
A base plate size should cover all the units with its outer periphery including the opening
A base plate is preferred to be designed concerning the body coordinate system (b.c.s).
A base plate should be drilled with datum holes / measuring holes in line with the pitch with 1000 mm in general.
The number of datum holes depends on the size of the plate, a minimum of 4 holes is required.
Datum holes should be drilled with nominal values of coordinate and in terms of 50mm and 100mm in general. ex -x200,y100,z300 .
Datum holes should be drilled with dia 100 mm away from other units.
Datum holes should be covered with datum plates.
- c) As a designer, it is important to know how big base plates or bigger base welded structures will be handled during the fabrication & handling process. The special case needs to take care of flatness if the base size is very long.
- d) Depending upon the weight eyebolts size is selected for lifting holes on the base plate. Generally, 4 eye bolt provision is made. You also need to select the location of the eye bolt considering the rope/belts used while shifting the structure or complete fixture are not damaging any units nearby.
- e) Most of the OEMs make 4 dowel holes & put a small aluminum plate marking the X, Y, & Z coordinates of dowel holes. If the base length is too long few OEMs follow the methodology of having holes at a 500mm distance.
- f) The best unit of the fixture must be strong enough so that the deflection of the fixture is as minimum as possible. This defection of a fixture is caused because of forces of welding, and clamping of the workpiece.
- g) The base unit of the fixture should have the mass to prevent vibration & chatter.
- h) The base unit may be built from a simple section so that other units may be fastened with screws or welded as necessary.
- i) Those parts of the fixture that remain permanently with the fixture may be welded. those parts that need frequent changing may be held with screws.
- j) The base unit should be parallel to the floor, to adjust this there should be provision of the height adjusting mechanism.
3. What is a Dump unit?
A dump unit is mostly used on difficult panels where the welds are not achieved easily. Sometimes, it happens that some hard-to-reach panels cannot be fixed by simple units, in such cases, fix them we use a dump unit.
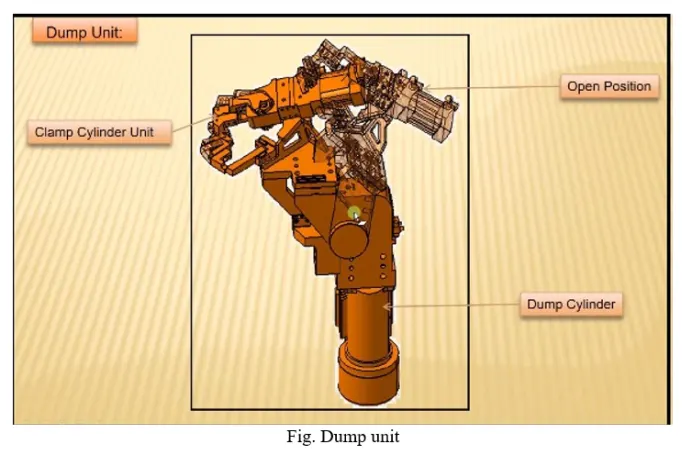
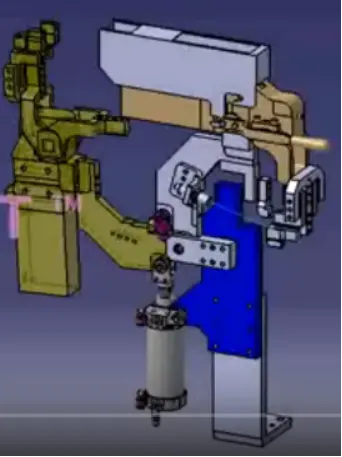
The first cylinder dumps the assembly carrying clamp mylars, and pins and then this assembly performs the required operation. In this unit, we should make sure that in the open position of the panel, we should be able to remove the panel.
Functions of Dump unit:
To ensure proper resting of the panel being welded and to restrict its motion.
A dump unit should have two cylinders one is to clamp the mylars at the localized point and the other cylinder is used to dump the whole unit.
In the dump unit, one assembly is fixed and that whole fixed assembly will mount on the dump unit cylinder.
Programming is the main part of to function dump unit. Because when the two cylinders move at the same time it causes distortions to the panel. So at that time programming will play the role.
Cylinder validation is more important in the case of a dump unit as the weight can be too heavy for the cylinder to dump.
In such a case, calculations are done and the force exerted by the cylinder is checked against the weight of the load being carried. If the cylinder force is more, it is validated or we use a more powerful cylinder.
4. What are the points you need to consider while designing a Dump unit?
The following points are needed to while designing the Dump unit.
1) Dump units are used when we can not use normal units like clamp units, pin units, etc. Due to some space constraints. The designed parts should be small in size but can do their functions effectively.
2) It contains the dump cylinder which will be the heavier part in all the units, The riser & blade should have enough strength to bear the load of the cylinder & all the units as well. The riser & blade thickness should be more in this type of units.
3) The parts should be designed by considering the open condition of the unit. In the open condition of the unit, the parts should not fall into another unit.
4) We can use any cylinder in this case that suits our requirements. In the below image of the dump unit, Both clamp cylinder & hinge cylinders are used.
- We need to ensure that the whole assembly being dumped should have less weight as possible without compromising on the strength of the parts. If we design the unit with very little weight there will be more possible to break the whole assembly. So design as much as possible to strengthen the design and more like reducing the weight.
- What is a Slide unit?
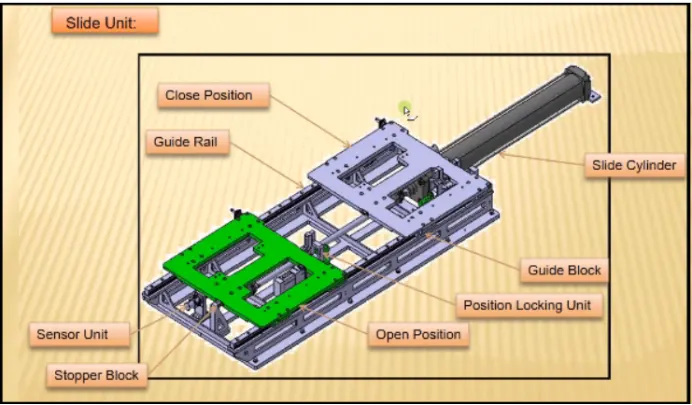
- A slide unit is a positioning unit that is used to position the car parts, panels, units, and robots for further operation.
- A sliding unit may consist of a pin unit, clamp unit, or rest unit depending upon the requirement of the fixture.
- A sliding unit is used where the geometry of a part is complex and also there are geometric constraints.
- The sliding unit has a cylinder that pushes or slides the unit forward and after completion of operation, it slides back to the original position.
- The sliding unit assembly is mounted on a plate that is moved back and forth with guide rails.
- The slide unit has sensors at the end to sense the position of the guide.
- The slide unit has stopper blocks to stop the movement of guide rails at particular positions.
- Slide units are classified into two types based on the guideways that are hardened guideways and LM guideways.
- Slide units may be further classified into three types based on prime mover used as manual slides, hydraulic/pneumatic slides, cnc slides.
- Slide units may be further classified as horizontal, vertical, and angular slide units depending upon their application .
6. What are the points you need to consider while designing a Slide unit?
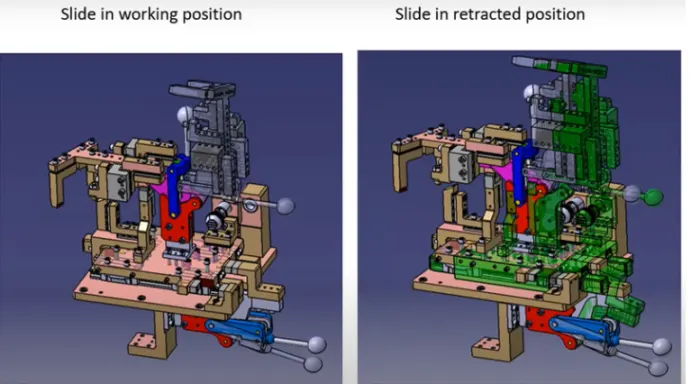
- Centre trunnion / rear clevis mounted cylinder is ideally used for sliding units as it allows some float to take up the misalignment.
- Reserve stroke of 10mm to be considered in both forward and retracted conditions.
- Cylinder and LM guide to be validated for load and stroke.
- LM guide rail length should be a standard and should be more than the actual stroke.
- Master guideway to be constrained and subsidiary guideway to be free.
- Mechanical hard stop to be considered for both extended and retracted positions.
- shock absorbers to be used for both extended and retracted conditions to reduce the impact of load.
- The slide is needed to be clamped or locked in a working position.
- Slide to be locked with a safety pin in the retracted position during transportation.
- The LM rails should be covered with sheetmetal or bellow to protect them against weld spatter or dust.
- The LM guide and rails are integrated assemblies and should not be separated at any cost.