Week 3:- BiW Fixture Design Methodologies Challenges
1.) Design Methodology
A three-phase methodology for the fixture design activity has been developed. The three phases include predesign analysis (phase I), functional analysis (phase II), and productivity improvement (phase III). In phase I, the product design information is studied, and initial fixture design aspects are developed.
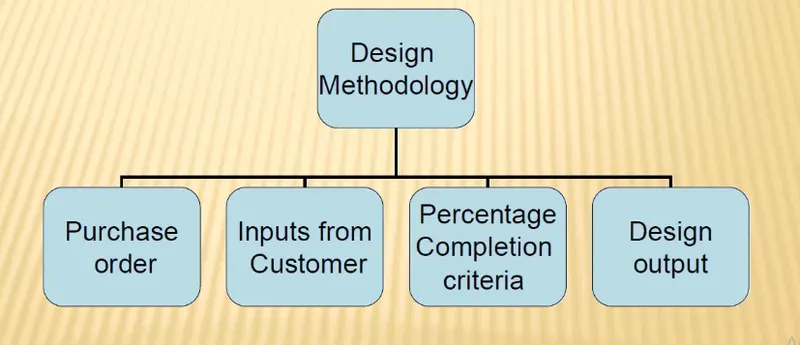
Design Methodology is divided into four sub categories:
- Purchase Order
- Inputs from Customer
- percentage completion criteria
- design output
Purchse Order:
A purchase order is the order from the customer end for the starting of the work. A purchase order (PO)is a commercial document and first official offer issued by a buyer to a seller indicating types,quntties,nd agreed price for products or services.It is used to control the purchasing of products and services from external suppliers.Purchase orders can be an essential part of enterprise resources planning system orders. Companies use purchase orders for several reasons. Purchase orders allow buyers to clearly and explicitily communication their intentions to sellers. They may also help a purchasing agent to mange incoming orders and pending orders. Sellers are also protected by pos in case of a buyer's refusal to pay for goods or services.
Purchase orders provide benifits in that they steamline the purchasing process to a standard procedure. Commercial lenders or financial institutions may provide financial assistance on the basis of purchase orders.
Inputs From Customer:
Inputs from customer basically are the data given by the customer like requirements,standards,layouts etc.
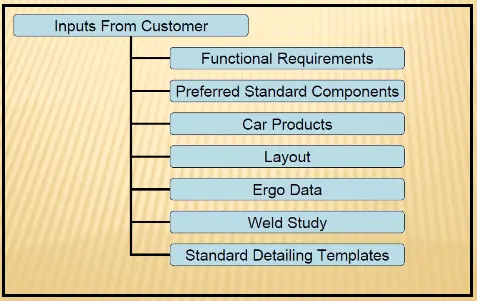
- Functional Requirements : The purpose of the function of the fixture will be given as input from the customers like what are the function the fixture is going to do i.e. welding,rivering,gluing,or whether it ie a checking fixture etc.
- Preferred Standards : As we know different companies follow different standards,followed by the customers. By following the standards in the time of designing and manufacturing of parts we will be saving the time and cost which will be automatically minimizing the time of the projects.As per the standars parts,it can be easily replaced from the used the fixture to the new fixture which reduces cost.
- Car Products: inputs we get from car products are GD&T,parts list ,CAD files of car part,clamp plan,produce assembly process sheet.
- Layout:Lay out shows the entire assembly plan to understand the process.Layout provides information of floe of parts,station pitch,robot station ,accessories like tool changes and tip dressers,sub assembly links,platform height,loading and unloading seqeunce heights.
- Ergo data : As same as preferred standards,different companies for the different standards of ergo data we have to customer standards of ergo data. The inputs of ergo dat will be the customer mostly in case of manually operated fixtures.The ergo data is mainly used to make the operator comfortable which may be lead to improve the efficiency in cycle time and production Data provides inputs like platform height,maximum and minimum treat from operator to fixture ,maximum and minimum height of the fixture ,whether the child parts or assemblies are visible while clamping for loding and unloading .Also provides information like loading height ,working safety zone of operator,etc.
- Weld study:Weld Study is the important inputs given by the customer: It gives details about the study of particular gun that we use for welding. Also like the number of weld, weld position of the components will be given. In short weld study includes welding gun details, weld Matrix and weld points.
- Standard detailing templates: These inputs include the detailing templates of 2D cad drawing as per the customer standards.So, we have to follow the detailing templates as per the customer standards.
Percentage completion criteria :
It is followed in designing stages and dispatch stages of welding fixtures.It Helps to track or identify how much task is completed and how much to go further for completing a fixture.
Input send concept design -0 to 25%
Concept approval and simulation check -25% to 40%
Design freezing and detalling -40% to 85%
check and final dispatch -85% to 100%
Design Output:
The otput is 3D models and 2D drawings of the tools
- Unitized tools : multiple units and their placements on the tool base.
- Layout sheets : a detailed drawing of individual units to include all of their components.
- Non utilized tools : tools that can stand alone and can be detailed completely on a layout sheet .
Hence, the design methodologies are explained in detail.
2.) Input required from the customer:
To start the desiging the fixture following are the inputes required for the desiging a fixture.
- Functional requirement
- preferred Standard components
- car product
- Layout
- Ergo data
- Weld study
- Standard detailing Templates.
Functional requirements:
The purpose of the function of the fixture will be given as input from the customers like what are the function the fixture is going to do i.e. Welding, riveting, gluing, or whether it is a checking fixture,etc.
It is one of the basic requirements to get from the customer to start designing a fixture.
Preferred standards:
As we know different companies follow different standards .we will be following the standards, followed by the customers. By following the standards in the time of designing and manufacturing of parts we will be saving the time and cost which will be automatically minimizing the time of the projects. As per the standard parts, it can be easily replaced from the used fixture to the new fixture which reduces cost.
Some of the preferred standard components used in BIW ar Stated below:
- Standards like ABB,NAAMS(North American Association for Mechanical Standards),DESTACO,ZYTRAN,TUNKERS.
- Standard Parts like Risers,L-Blocks,Retainers,Pins.
- Components like Clamps,Cylinders,Slides,Switches,Sensors.
- Weld guns,Tip Dressers,Tool changers-Tip Dressers are used to sharpen the tip of the tools which are used in robots in various process.
Car Products:
The inputs we get from car products are: GD&T part list, Cad files of car part, Clamp plan, product assembly process sheet.
- GD&T: It provides information of locating pins, rest, clamp, damp & slide unit information of each station .Also includes the information of sequence of openings of clamps, dumps & slide stroke information.
- Part Lists: It gives the lists of parts which are going to be assembled inthe fixture. The list contains the information of part number, part name, revision of fixture, part thickness, etc
- Clamp plan: Clamp plan provides the information of location of pins, Rest units, clamp unit, dump etc. It is the important input from customer. The clamp plan/position should not be changed without the knowledge of customer
- 3D cad file: The 3D model of the car part will be given the customer, From that 3D model we will be developing our fixture design process. The 3D cad file will be in the format of step file (stp) or IGES file igs)process. The 3D cad tile will be in the tormat ot step tile (stp) or IGES tile igs).
- Product assembly process sheet: It gives the information of stage wise assembly process like how the parts move from one assembly process to other after the completion of joining process.
Layout:
Lay out shows the entire assembly plan to understand the process. Layout provides information of
- Flow of parts,
- Station pitch,
- Robot stations,
- Accessories like tool changes and tip dressers,
- Sub assembly links,
- Platform height,
- Loading and unloading sequence heights.
Ergo data:
As same as preferred standards, different companies for the different standards of ergo data. We have to follow the customary standards of ergo data. The inputs of Ergo data will be given by the customer mostly in case of manually operated fixtures. The Ergo data is mainly used to make the operator comfortable which may lead to improve the efficiency in cycle time and production. Data provides inputs like platform height, maximum and minimum treat from operatorto fixture, maximum and minimum height of the fixture, whether the child parts or assemblies are visible while clamping for loading and unloading. Also provides information like loadlig height, working safety zone of operator,etc.
Weld study:
Weld Study is theimportant inputs given by the customer. ltgves details about he stud/ oi par#cular gun that we use for welding
Also like the number of weld, weld position of the components will be fn In short Weld study includes welding gun details. weld Matrix and weld points.
Standard detailing templates:
These inputs include the detailing templates of 2D cad drawing as per the customer standardsSoj we have to follow the detailing templates as per the customer standards.
Hence,inputs from the customer to start the desigining of the fixture are explained in detail.
Q3.) Car Product:
Inputs we get from car products include:
- GD&T
- Parts lists.
- 3D cad file
- Clamp plan.
- Product assembly process sheet.
Geometry Dimension and Tolerancing:
It provides information of locating pins,rest,clamp,damp & Slide unit information of each sttation.
Also includes the information of sequence of openings of Clamps,dumps & slide stroke information,
Part List:
Part list gives thee information of parts in a unitit consists of part number,patt name which helps to ientify the part easily,number of parts required and its thickness.this list helps to check all the parts and its dimensions and required number of quantities.
CAD files of the car part:
CAD files of car parts gives the simulations of those 3D models and their analysis.lt is also used throughout the engineering process from concptual design and layout of products through strength and dynamic analysis of assemblies to definition of manufacturing methods of components,
Clamp plan:
This is the clamping plan while doing the operation-We cannot complain without permission of the customer.lt is very important input from the customer.lt provides location of pins,rest,clamps,dumps,etc.
If the clamp is nearer to the weld spot,one should not chang the clamp position withou consulting It even it appears to damage the clampor the tooLDestgn should not change without consulting with superior,
Product Assembly Process Sheet:
It gives detail process of the completion of the part from scratch to the finished productof the assembly.
Product assembly process sheet gives complete assembly of a unit.Different parts iri a unit are assem>led by geo weld first.Then the weld parts are assembled by re-spot welding-Similarly,everysmall part)0f a prpduci or unit is assembleåfirstand !hese small parts are welded together to get a final product.
Hence,these are the inputs we get from car products.
Q.4) Clamp Plan:
Clamp:
A clamp is a fastening device used to hold or secure objects tightly together to prevent movement or separation through the application of Inward pressure.
Essential requirements of clamps:
All clamps must fulfill four essential requirements. They are,
- The work piece must be held rigid while undergoing operations
- The time required for loading / unloading the tool must be as short as possible, which means the clamping device must be quick acting.
- when subjected to vibration, chattered, heavy pressure the clamping must be positive.
- The clamp must not damage the work piece.
CLAMP PLAN:
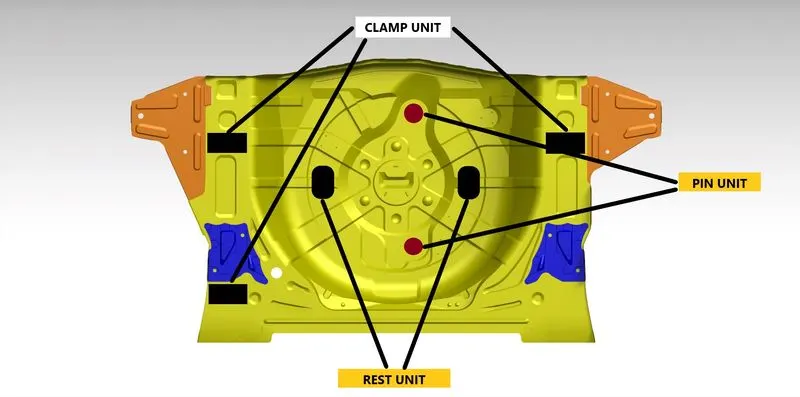
Clamp plan provides the information of location of pins, test units, ciamo unit cump etc.
It is the important input from customer. The clamp plan/position should not be changed with out the knowledge of customer.
It gives the detail of the exact position of the camping units by mentioning a co-ordin4Fs the particular position.
Clamp Plan is very important input that we get in the car products is where exactly we can place those clamping units are the particular pin Units.
We should never change the position of the particular clamp or the pin, which is given in these data.
We can change our design a little bit here or there, but we should not change the input design data about the clamp position or the pin position.
In the Clamp plan there is clamp unit ,pin unit and it is more detailed italso gives the exact location of Y and Z Coordinates designing as well you can just input these coordinates and you can start designing from there.
We should never change the position of the particular clamp or the pin, which is given in these data.
We can change our design a tittle bit here or there, but we should not change 'theinput design data about the clamp position or the pin position.
"In the Clamp plan thereis clamp unit ,pin unit and itis more detailed it also gives 'the exact location of Y and Z Coordinates designing as well you can just input these coordinates and you can start designing from there,
If the three coordinates whole diameter and everything is already given to design theentirefuture design phase, and it sometimes ministry as well, it happens that another thought position, also given very close to the clamp, or the clamp location. So always ask to whether you have changed the clamp position
You should never change the vent position or the clamp position without askingit so always be valvaboutthese situations So the tool might get damaged or department get damaged so for that itself needto clariiy once again before doing any changes in the clamp.
Hence, this is the clamp plan.
Q.5) Layout:
Layout:
Layout is basically an layout of the entire assembly line to understand the process flow of work.
Layout sheet wilt give you information about all the fixturesare placed the robots are going to work on it.
In layout sheet the circle around the robot is called trapped area of that particular robot,
So this is basically the reachability of that robot and which is confined to the particular circle
For example robot is going to work on the fixture details also mentioned the geo 250 and then number is given 250, and as you can see 250 02 so 'this is dueling to one or two it is going to use there sq this robot is going to work on the site first. Then after finishing the site. This fixture is going to rotate and then it will come to t 01, and these two robots are going to work on the other side of the fixture similarly this robot is also going to work on the particular component as we
this robot is also going to work on the particular component as well
Entire sheet will give you in that plan of the layout of what are the constraints that is there from the customer side itself.
If you want to do any changes for example you re changing the geo fixture design and it is gonna exceed a little bit bigger or smaller inside you have to inform the customer and you have to get the customers permission to co that so that he will also be able to change the design if we present him with anything.
Layout provides information about:
Flow of parts:
In the flow of parts how the particular component is going to move from one un!tto another of one station to another station
Station pitch:
In station pitch a distance between two stations. What is the space concept thattheyhave etween two stations.
Robot stations:
Robot stations and positions where the robot placed stations,
Accessories like tool changer and tip dresser.
Accessories like tool changes and tipdresser. So where are those also placed. So that is it the robot wants to change the particular tool, which it has to go to the parlicular location and change it.
Sub assembly links:
Subs assembly links are basically how the particular fixtures how the assembly fixtures are linked to the mala assembly line.
Loading/un(oading sequence/heights:
Platform height and loading and utiloading sequence of height.
Hence, this is the purpose of a layout.
Q.6) Ergo Data:
ERGO DATA:
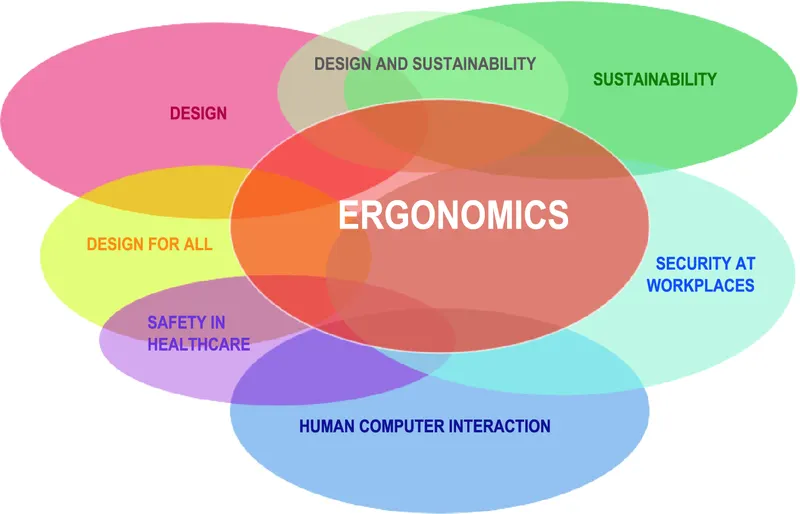
Ergo data is nothing but the data or Inputs Which gives the human factors engineering data, between the operator & his working environment. Before detailing about ergo data we should know about ergonomics in detail.
ERGONOMICS:
Ergonomics also known as human engineering & human factors engineering IS the scientific study of the relationship between man and his working environments.
OBJECTIVES OF ERGONOMICS:
The fundamental objective of the study of ergonomies is to optimize the!integration of man & machine so as to improve the productivity & accuracy.
In short, the objective of ergonomics is designing for human use & optimize Illi working & llVlng con ition.
Two main objectives of ergonomics are:
- To enhance the efficiency and effectiveness with which the work carried outs as oin reasei he convenience of use, reduced errors & increase in productivity
- To enhance certain desirable human values including safety, reduced stress fatigue and improved ?gality of life.
Ergonomics involves the design:
- Work place suitable for the worker.
- Machinery & controls, so as to minimize physical strain on the worker to enable the improvement in the efficiency,
- An environment for performing a task most effentively and conducive
- A conducive task and work organization.
Benefits of Ergonomics:
- Improved working condition.
- Reduce physical workload.
- Improved work postures,Reduced efforts of certain movements.
- Better reading instrument displays, handling of machine levers & Controls.
- Reduced unnecessary information recall efforts.
The twelve ergonomic guidelines resulting from the workshop with the engineers were incorporated into the design requirements:
- Flexibility and adjustability for viewing angle, access, and handedness, eg. Whele possible, a fixture rotates, changes angle, tilts. Physical access (space) for hands or tools and clear visual viewing angle.
- Prevent blind assembly.
- Eliminate obstruetions in front of working area for ease of access e.g.(knob position).
- Standardized light colors e.g. Yellow In process, green — complete,red-fault.
- Locate lights as close to hand location as possible.
- Design should not rely on operator 'for positioning.
- Ensure operations do not cause change in positioning of part i.e.The need stablization by person.
- Avoid having to hold with 2nd hand while loading.
Q.7) Weld Study:
Weld Study:
Weld study means a study of the welding technique that we are gooing to use,its temperature,type of current,type of gases used,type of gun used for welding and where are we going to weld etc.lf we use a spot welding what kind of electrode is used for welding,number of spots etc, come under the weld study of that particular component
Weld Study includes:
- Weld gun details.
- Weld matrix and weld points.
- Geo weld points and respot weld points,
- Weld gun details.
- Weld matrix and weld points.
- Geo weld points and respot weld points,
Weld Gun Details:
- This involves the study of the gun like
- Type of weld it does
- Number of spots it can weld e Temperature of the weld.
- Type of current used
- Approach of the gun.
Weld matrix and weld points:
Weld points are basically where the welding is going le lappen at which point at which coordinates is gotng to happen.
Geo weld points and Respot Weld Points:
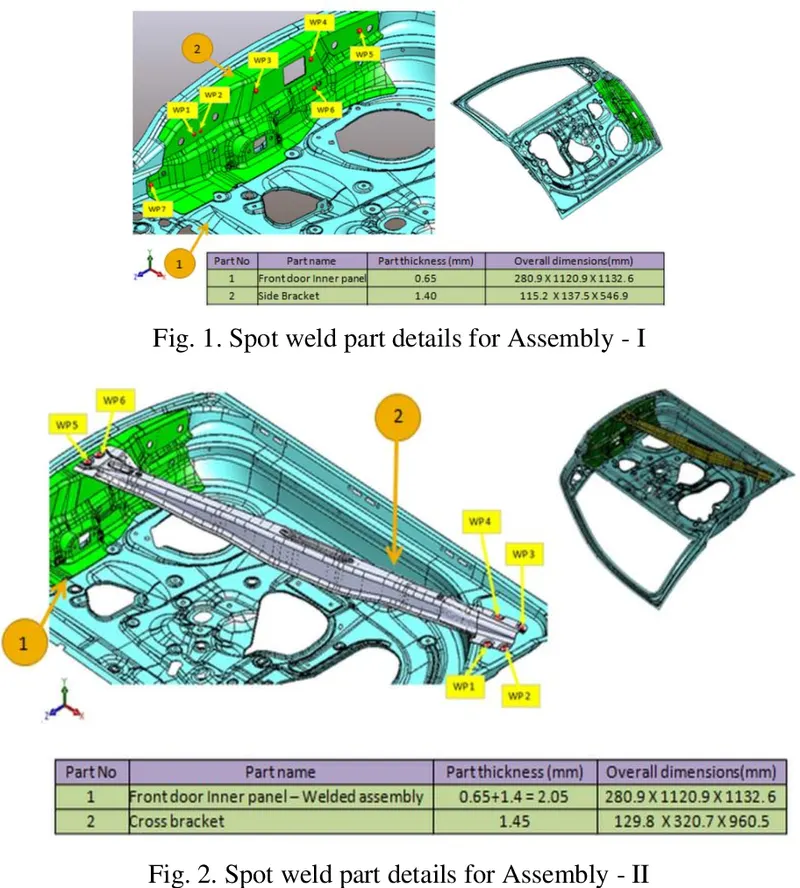
The data of weld metrix and weld points will be given to you in the formof Spheres i.e, red and green spears.
At that points welding 'is going to happen.
Geo spots are Red in Color and Re spots are Green in color.
All the red spheres are going to happen in geostationary.
In the respot station where the green welding is going to happen.So this happens where one component is going to attach to this particular component, and in the other station, the other component get attach.
Q.8) Criteria for percentage completion in the designing stage:
The percentage completion criteria is followed in the designing stages and dispatch stages of welding fixtures.
This percentage completion criteria is followed totrace the project whether it matches the committed date given to the customer for hand
Also it helps us to identify the stages in theprojects like how much the is completed and what are the further stages are in pending to complete which helps us tocomplete the projects on the committed time and date.
The percentage completioncriteria is divided into four stages to identify the p%entage of the completion of work
The four stages of percentage completion criteria are as follows:
- Input & concept design
- Concept approval & simulation check
- Design freezing & detailing
- Check & final dispatch
Input & concept design:
This is Initial stage of project. Input data provided by customer like 'functional requirement, customer standard etc. & after studying those inputs the concept of fixture design is created. After completion of this tasks about 25% of work completed Concept approval & simulation check:
As concept of fixture design is created & simulation checked it is sending for customer approval Customer will study all simulations & gives his approvaL If there are any changes required, then it has to do accordingly & again submit for approval This concept design approval from the customer after study of simulation contributes only 15% of total design work. But with completion of this task 75-40% works completed.
Design freezing & detailing:
This phase involve design freezing after approval of concept design Freezing means finalizing concept design. Then next step is detailing as
I ms pnase Involve design Treeztng arter approval ot concept design Freezing means tinaunng concept aeslgn. I nen next step IS detailing as per customer standard template. With completion of this stage almost 85% of work is completed in designing stage.
Check & final dispatch:
After detailing the quality checking team starts inspection of all the date it will dispatch to the customer litis ok as per customer standard.ff there is in error in drafting it will create Issue or mistake in manufacturing stage. Thus, a percent completion criterion helps us to know where we are in design process.
Q.9)"Output" in design:
It includes data to be given to customer after completion of design stage. The qtpyt is 3D models & 2D drawings of the tool.
In the fixture element design output contains delailed design of locators etalled des' of damps, detailed design ofsupports positions of locators, positions of clamp,positions of supports if any type of locators, types of clam , types ofsupports, Claring forces & supports.
There are two types of tools in fixture design:
- Unitized tool
- Non unitized tool.
Unitised Tool:
In unitized tool there are multiple units on common base for example geo ixture rauotlixture, checking fixfure, hemming station etc Unitized tools require two types of sheets:
- Key sheet: An index of units & their placement on the tool base. e sheet show (acemeot& location of that particular unit on tool base where exactly & exact position of tool base. eys eet is s owing orthogonalorisometnc 'ie of that entire component.
- Layout Sheet: A detailed drawing induadual unit to include all of their unit . Layout sheet detail drawing of that particular tool where we are going detils of components . This also helps in CMM inspection of fixture.
Non 'Unitised Tool:
Non-unitized tools that can stand alone & can be detailed dodely on a a out sheet.Cgu Rack, take out rolleys, tum tables, grippers etc.
The output should compile following point:
- Approved standard parts should be used wherever possible. This saves lots of ti e, efforts & economical
- Design should be as simple & economical as possible. Geometry is complex but approach is trying to design as simple possible.
- Design must comply with all current safely & ergonomics standard.
- Design must provide for controlled & damage free handling of product. It should hdt damagf other part.
- Adequate error proofing provision must be incorporated in each design by providing proximity switches, rough locatore ele. Proximity switches are basically sensors which tells part is present or not in fixture Rough 'locators work as poka yoke to guide entire panel orientation.
- The weight of moving part must be kept to minimum while maintaining maximum strength .welght of moving component kept as minimum as possible but it shouldn't compromise on strength. There is balance between these two things.
- Frames & structures are to be simple & sturdy.
- Design clearances and accessibility for routine maintenance & service. Fixture need to maintain after certain period of time so it is easily accessible for maintenance.
- Motion control must be considered on any moving component. Adequate to control the motion of component like slider,clamp alarm so that it does not give any vibration & stays on particular 'it by use of hard stopper shock absorber,
- Designer is responsible to validate all clamps & welding guns.so that all clamps & gun should perform its function without fail.
Q.10) Stucturing a Design Tree:
Structuring a design tree:
A process where all the assemblies and parts are named in a specific standard Different customers have different set of standards and the
Every company,every customer has different standards of their own structural design tree.
so they will be giving a template on how the structuring and detailing of the design is do e. nd you have to follow that particular designing
In the design tree itself if we mentioned that particular name, wherever that part is We can easily know that this part belongs to this one or this station or this assembly on particular unit. So this helps us to avoid errors during the design study, manufacturing assembly and inspections.
Structuring a design tree is actually to avoid the errors, which might come 'during manufacturing assembly, or either in house inspections as well
If the part, or assembly are not named properly, or design tree is not structured properly, itwill create confusion to understand the design and may create major possibilities of making an error.
Every part, every component should be named according to their procedures.
If we did a mistake or renamed the entire standard parts from the customer as a design partuNowtÅe customer is going to manufacture the entire part again from the scratch, but he already have that product in his iPnerary.but exte cost extra time and is feasible. This is also known as an error which is actually going to increase the cost of the entire assemßly as well
Naming a fixture or a unit or a part gives the information as to which project zone or assembl Yo they belong.
If we name the part properly or name the fixture properlyillactvally tell yhich unit or which assembly o which zone or in which station it actually belongs
It can help us to identify the quantity of items of same types prdifferenF types that a e be pg used in an assembly.
In design tree in which designed parts are at top & all standard parts are at bottom.
The blue highlighted number is HIL-T9A-RRFRA-JG3-OO-OO-OO
- HIL-T9A -The project name
- RRFRA - Panel name JG3 -Jig noB 00 - unit no
- 00 - Part no.
00 - Component no.
Under the product there are main assemblies, sub assembled child part stan ard parts ,etc . these all parts are provided with specific number, zone etc. to identify easily.
Q.11)
Units:
A unit is a device that has a specified functionrespecially one forming art of a complex mechanism-multiple units are joined together in order to form a fixture and are attached to a common base,which serves as a common support to the units where they are fixed.
A welding fixture is assembly of different types of units.
As name refers,the different units each serves with different functions and different purposes.
Units are classified into two types:
- Unitised tools
- Non unitised tools.
IUNITISED TOOLS:
Unitized tools are basically tools Which are a art of multiple units or multiple tools ihside of it These are the toots which has to be represented by two formats i.e. Key Sheets and Layout Sheets.Unitized tools are basically two types:
a)Simple units:
Simple units will have a very simple design to it,then the approach of the deesigntng and manufacturing is also very simplistic-Simple units are classified as.
- Rest unit: Rest unit is basically a unit where the component is teste ,there,is no upper clamp toit,theere is no force applied to it-There is no cylinder attached to it,usually it will have a riser, a blade ane few rest mylers.
- Fixed pin unit: fixed pin unit is basically a unit which has ap n which fixed:itcannot be moved.
- Retract pin unit: Retract pin unit is opposte to fixture which can be move up' and down by using a etracable pneumatic cylinder,so it can be retraced to a certain distance.
- Rough Locators: A rough locator is a part designed to guide the the carpanelon the pins accordinglyA rough locator can be of standard part or make part.
- Sensor Unit A sensor units are used in actually sensing whethe the pnel or a particular component is there or not-For example if we are assembling component of 10 parts,Each part will have a sensor or,multi eattached it.
- Base unit: A base unit is a uni't designd to mount all other units.
b)Complex units:
Complex units,like slide unit is an example of a comlex unit thatdesign itself a little cpmplex In design.
- Slide unit :The slide units are basically where the sliding mechanism is involved.
- Dump Unit : Dump unit is basically like a conveyor Where we assemble a com onent if we have a particular constraint
2.NON UNITIZED TOOLS:
Non unitized tools are basically one unit itsef which is basically don't have any process functonality to it is just to keep component on it as a stabl ,like grippers turntable,stands,etc.Non utilized tools are:
- Stands
- Take out trolleys
- Conveyor
- Turn table
- Some grippers.
Q.12) Fixed Pin Unit:
It is design to car locate panel usign pins. It is aleready fixed and it cannot move up and down.Below are the different parts pin unit in general.
- Pin
- Pin retainer
- Shims/spacers
- Block
- Blade/adoptor plate.
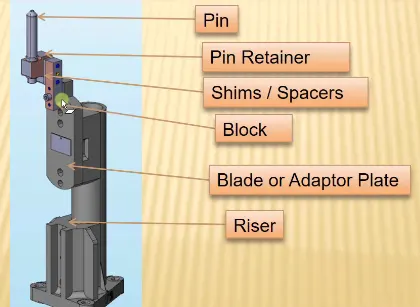
Every pin unit will have two directional shims.The block is used to mount entire pin unit. Shims are used to avoid stackup tolerence while assembling entire component. shims come in pack of 0.1,0.2&0.5cm.
Purpose of Fixed pin unit :
Pin is most important part of fixture & used to restrict rotational as well as translational degree of fredom of tht prticular component . Purpose of fixed pin unit is to panel translation motion along two axis and to prevent rotational of panel in the axis of panel.
Q.13) Diffrent parts of a Fixed Unit:
The different parts of a fixed units are:
- Locating Pin
- Pin Retainer
- Shims
- Blade
- Riser
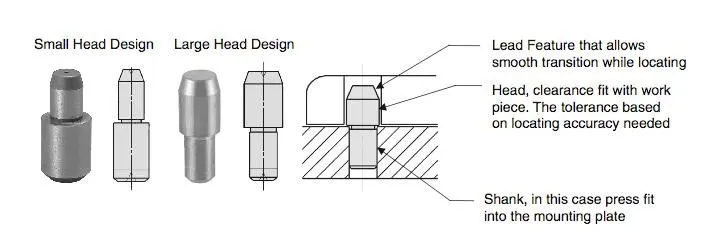
Locating Pins:
locating pins are used for controlled ,fine tolerance positioning of a work piece. Usually two locating pins are used to properly locate the work piece on one plane. There are dozens of styles of locating pins that can be utilize a design.
Locating pins are great way to locating sure the prts are putting togethr fit they want to fit it . Drill two holes opposite to each other in each part installed a cylindiracal locating pin ,parts are aligned exactly the way we want . if we are having alignment issues with using just bolts or other fastners,a locating pins can be a great way to form up or assembly.
Risers:
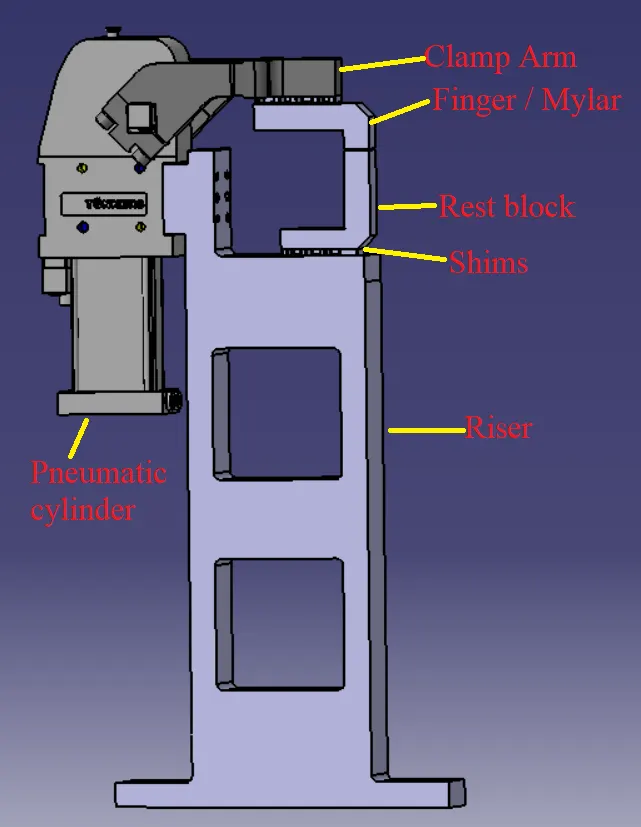
Risers is structure generally used to mount the toggle clamp & rest ,clamp mylars and location pin.
It is not necessary to have one riser where all the parts of clamp & rest or location units are mounted.
Generally risers are either made of plate fabrication of plate and tube welding together or from single gas cut plate.
These are generally manufactured to give height to the assembeled.
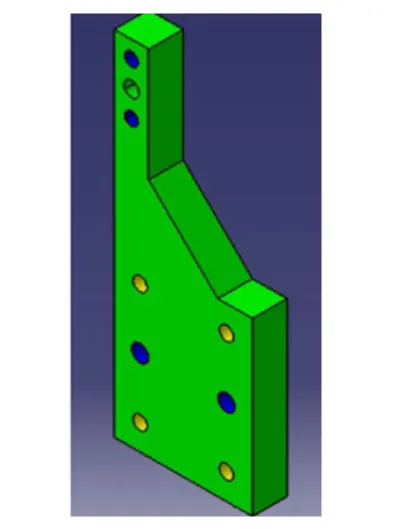
Blade:
Blades are the plates attached to the riser. Parts like cylinder,arm etc are mounted on the blad . chamfer is given to straighten to the blade.
Shims:
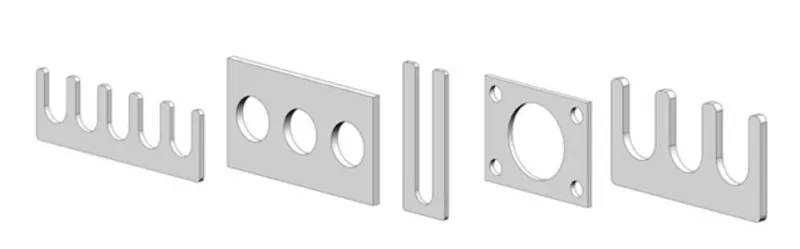
Metal shims are used to finely adjust the location of how the fixture holds the product so that it is welded together within the dimensions set for the product to work well.
A pack of thin metal sheet is placed between two components in the fixture.The fisrt component is fixed place and second component is attached to the first component with the pack of the shims in between. Removing one shim or adding one shim slightly adjusts the location of the second component. This is important to the manufacturers who want to have their producte's parts assemble easily after being welded.
Pin Retainers:
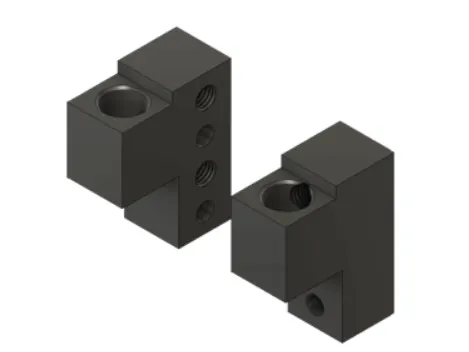
A pin retainers is a part which holdes the pin in position ,the pin retainer can be either a make a part or a standard part also .Pin retainer is used to hold the locating pins firmly.
Hence, these are the different parts of a fixed unit.
Q.14) Rest Unit:
Rest unit is unit designed to support car pnel using Myler/NC block /rest component is rested only ,no upper clamp or force applied there. It is the simplest unit design because it has fewer part to design & purpose to the only resting car panel.
It can be combined with clamp unit to clamp as well as to rest the car panel.It can be combined with locating unit to locat as well as to rest the car panel .Also locating ,clamping and test unit can be combined unit to reduce cost.
There is no unit to attached it.it has rest Myler ,blade and rise & below is differnt parts of rest unit.Rest unit is also devided into simple support,units & retractable support unit.
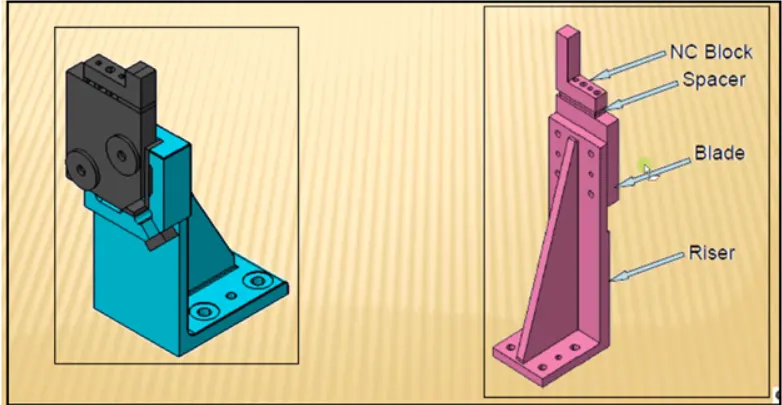
The different parts of a Rest unit are:
- NC Block/Mylars
- Spacers
- Blade
- Riser
NC Block/Mylars:
Mylars are the part which are holding the panel from top & bottornlt is a jaw8pe,duræwelding i€wont deforms from its position.lt is also known as fingers.lt wpnt allow the deformation of the part due to stresses.
Mylars are of two types,they are
- Clamping mylars
- Resting mylars
Only resting mylar are seen in resting unit .The panel which Qnstsant the part is nown as resting mylars.
Risers:
Riser is a structure generally used to mount the toggle clamp and rest, clamp mylars and location pin.
It is not necessary to haveone riser where all the parts of rest or location unity are mounted.
Generally risers are either made of plate fabrication or plate and tubewelding together or from single gas cut plate.
These are generally manufactured to give height to the assembly.
Spacers/Shims:
Metal shims are used to finely adjust the locationof how the fixture holds the product sogthatit is welded together within the dimensions set for the product to work well.
A pack of thin metal shim is placed between two components in the fixture.The first component IS fixed in place and the second component is attached to the first component withfthe pack ofsfiims in between; Removing one shim or adding one shim slightly adjusts the location of the second component is important to manufacpurers who want iolnave their produds parts assemble easily after being welded.
Q.15) Sensors:
Sensor unit:
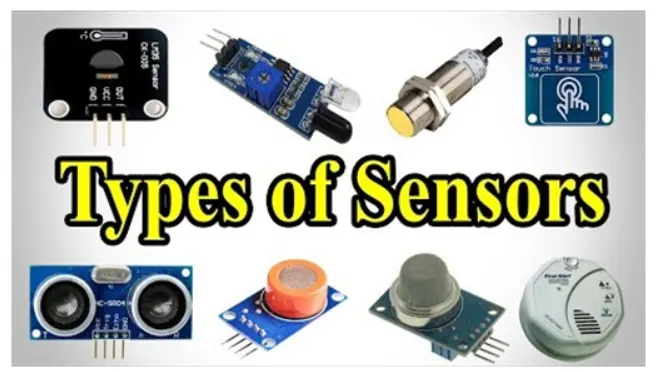
A sensor is a device that measures physical input from its environment that can be interpreted by either a human or a machine Most sensors are electronic (the data is converted into electronic data), but some are more simple, such as a glass thermometer, which presents visual data, People use sensors to measure temperature, gauge distance detect smoke, regulate pressure and a myriad of other uses.
Types of Sensors used in general are:
- Proximity sensors
- Photo electric sensors
- Laser sensors
Proximity sensors:
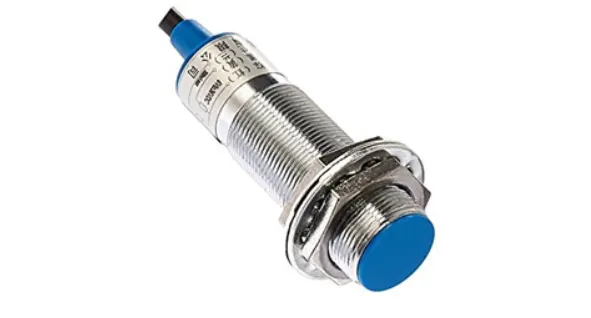
A proximity sensor is a non-contact sensor that detects the presence of an object the target enters ,the sensor's field. Depending on the type of proximity sensor, sound, light, infrared radiation (IR), or electromagnetic fields may be utilized by the sensor to detect a target.
Proximity sensors are used in phones, recycling plants, self-driving cars, Anti aircraft system assembly lines. There are many types of proximity sensors, and they each sense targets in distinct ways. The two most common used Proximity sensors are the inductive proximity sensor and the capacitive proximity sensor.
An inductive proximity sensor can only detect metal targets. This is because the sensor utilize an electromagnetic field. When a metal target enters the electromagnetic field, the inductive characteristics: of the metal if change the field property alerting the proximity sensor of the presence of a metallic target. Depending on how inductive the metal is, the age target can be detected greater or shorter distance.
Capacitive proximity sensors, on the other hand, are not limited to etc. These se anything that can carry an electrical charge. Capacitive sensors are commonly used in liquid level detection.
Photoelectric Sensors:
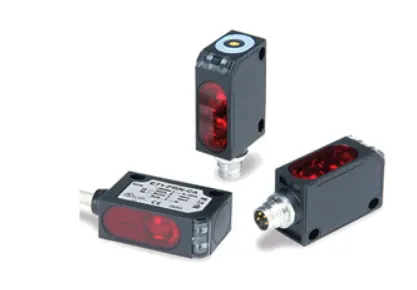
Photoelectric Sensors detect object change in surface conditions, and other items through variety of optical properties. A Photoelectric
Sensor consists primarily of an Emitter for emitting light and a Receiver of receiving interrupted or reflected by the sensing object; 'it changes the amount of light that arrives at the Receiver. The receiver detects this change and converts it to an electrical output. The light source for the majority of Photoelectric Sensor infrared or & invisible light (generally red, or green/blue for identifying colors).
Laser Sensors:
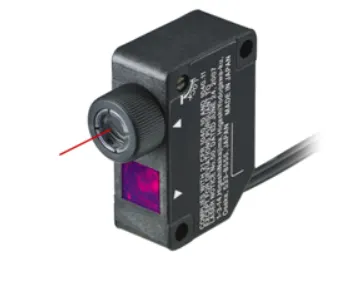
These laser distance sensors use a focused, coherent light to measure distance to target object in factory automation
applications, the target is usually a product machine element. They detect any solid object an produce an output proportional to the measure distance independent of material color and brightness. The high resolution output distance sensors is used to provide position or displacement, usually to the input of some type of industrial controller ,such as PLC is often highly accurate ,and include.
includes temperature Compensation to enhance are several types of laser distance sense some including diffuse,
Fundamentals of Sensor Design:
- Every single loose panel, which are being welded in a tool should be Sesed.
- Each panel should be sensed by one or two sensors diagonally opposite ends of the panel
- If a component is really small, we need not use two or three sensors for that you can use one sensor to detect the particular panel.
- If the panel is really big, we will use two sensors in opposite directions to sense the panel.
- So every sensor should be mounted in three directional adjustable ways in general.
- Sensor manufacturers are IFM, Peperl-Fuchs, OMRON etc.
Q.16) Rough Locator:
Rough locator are the element that aim the operator to guid the car panel while loading on to the fixture and ensure full proff assembly.
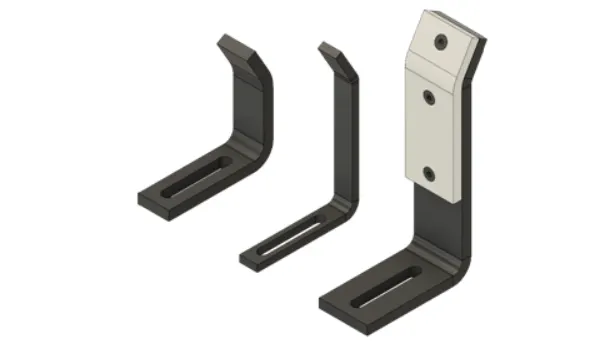
It is used a fool proofing method, because due to the rough locator part cannot be located in correct position. The rough locators are set according to the respective panel. Hence, art can only be loaded in defined direction and orientation.
FUNDAMENTALS OF ROUGH LOCATOR DESIGN:
- Rough locators should be placed at the edges of the car panel which it has to guide.
- Rough locator has to be placed at the same angle of the car part edge with a minimum distance of 2.5mm from the edge of the car part.
- Rough locator should guide the panel in the pin arresting direction,
- Rough locator should guide the panel before 10-15 mm to start of the pin engagement
- Rough locator should be designed with entry angle for the car panel. Generally It ranges betweenBO-45 degree. Rough locator should be designed with two slots to mount-the easy adjustments
- The locators should be in the direction of car part guiding.
Q.17)
Base unit:
A base unit is the unit designed to mount all the other units (clamp unit jn unit, Rest unit etc) of the tool, also other parts necessary for tool pneumatic valve box, trunking cable path will also be mounted onto a base unit. 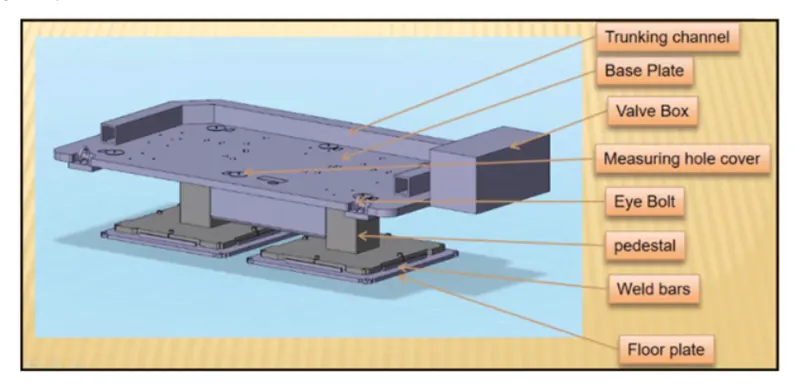
Parts of Base unit:
Parts of base unit are as follows:
- Valve box
- Trunking channel
- Measuring hole cover
- Eye bolt
- Pedestal
- Floor plates.
Valve box:
Valve box is basically a box which supplies air to all the pneumatic cylindehs assembled 'n the fixture. Valve box consist of one solenoid valve is used to collect the air from 'the pneumatic cylinders to valve box.
Trunking channel:
Trunking channel is a kind of cable duct. which helps to guide and protect the wirings) •tåbes' used in khe fixtures, Measuring hole cover:
In the measuring hole cover the coordinates points are engraved on it.
The hole which mention the coordinates gives the position placements of the particular units.
The measuring hole helps in CMM inspection & QC inspection.
Eye bolt:
An eye bolt is a bolt with a loop at one end They are used to firmly attach a securing eye to a structure, so that ropes of cables may then be tied to it for lifting purpose
Eyebolt IS used to frag or lift the base unit while relocating.
Pedestal:
Pedestal is a stand like structure where the entire unit of the base will be mounted. Floor plates:
Pedestal is a stand like structure where the entire unit of the base will be Floor plates:
Plates used to mount the entire base with floor,
Alsob4ps to achieve the flatness soft the fixture.
Hence , the base unit and their parts are explain edindetaiv.
Q.18)
Dump unit:
Dump unit is where you assemble component if you have certain constraint: you will( have clamp unit, pin unit attached panel will be assembled. So if you have certain constraint you cannot assemble in normal way. Dump different way, It has dump cylinder & complex design It consists of dump cylinder to perform the operation of clamping & unclamping car panel. A dump unit can have more than one cylinder to perform such operation. The first cylinder dumps the assembly carrying clamp Mylar, pins and then this assembly performs the required operation in this unit, we should make sure that in the open position of panel, we should be able to remove the panel.
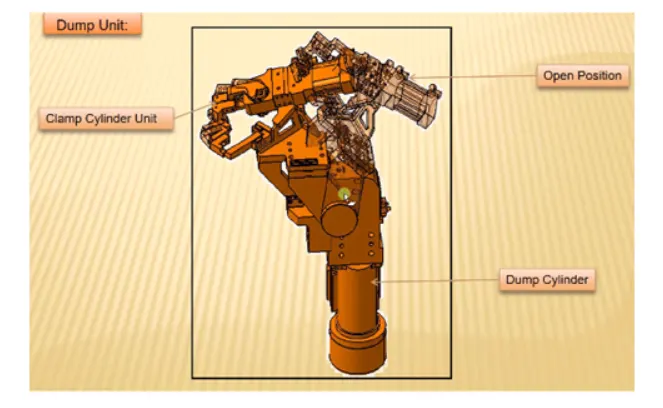
Functions of Dump Unit:
If you have particular constraint and you cannot assemble in a normal way to use this use it in different ways again it has same dump cylinder and it has open position and closed position and it has Clamp Cylinder Unit too.
That is why these are very complex and design.
If you have any geometrical constraints, you can use this dampener to constrain your components.
Q.19)
Slide units:
Slide units are positioning units, which are used to position the car part or panel, units, we(d gup, robots for further operations. Slide units may be classified into two types based on the type of guide ways, They are,
- Hardened guide way.
- LM guide way
Slide units may further classified into three types based on the prime mover, They are,
- Manual slides.
- Hydraulic/pneumatic slides.
- CNC slides.
It may be further classified depending on the application as.
- horizontal slide unit.
- Vertical slide unit
- Angular slide unit.
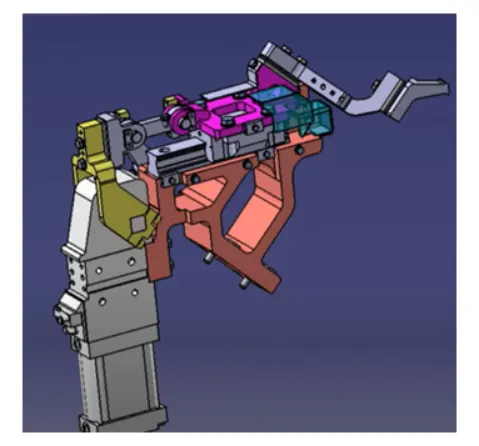
Basic fundamentals of slide unit design:
- Reverse stroke 10mm to be considered in both forward & retracted condition.
- Cylinder & LM guides to be validate for load & stroke.
- Master guide way should be constrained & the subsidiary guide way to be /ree.
- Mechanical hard stop to be considered for both extended & retracted condition.
- Shock absorber should be used for both extended & retracted condition to reduce impact load.
- Slide to be locked/clamped in the working position.
- Slide to be locked with a safety pin in the retracted position during transportation,
- The two end limits to be sensed externally by a proximity switch
- The design should be checked for screw accessibility, ease of assembly, machioability of parts.
- The LM guide & rails are integral assemblies and should not be
- LM guide ways to be lubricated for long life.
Hence these are slide units.