Week 2:- BiW Fixture Basics Challenge
1.) Project Activities:
- RFQ Recived
- Specification discussion meeting
- Offer subimission
- LOT/PO receipt
- Schedule preperation
- BOM preperation
- Design concept preperation
- Customer approval
- Detaling and drawing release
- Manufacturing/ BOP ordering
- Mech/Elec assembly
- Quality inspection
- Internal trail and testing
- Online trial
- Packaging
- Dispatch
- Installation
- Trail and training at customer
- Off meeting
- Final handover
2.) Types of joining proess:
Two fundamental options for joining materials and components.
1> Mechanical joining
2> Metallurgical joining
Metallurgical joining:
- Resistance spot welding
- Resistance seam welding
- Resistance projection welding
- Arc welding
- MIG welding
- TIG welding
- Submerged arc welding
- Plasma arc welding
3.) Resistance welding:
Resistance welding is a welding technology widely used in manufacturing industry for joining metal sheet and components.
Types:
- Resistance spot welding
- Resistance seam welding
- Resistance projection welding
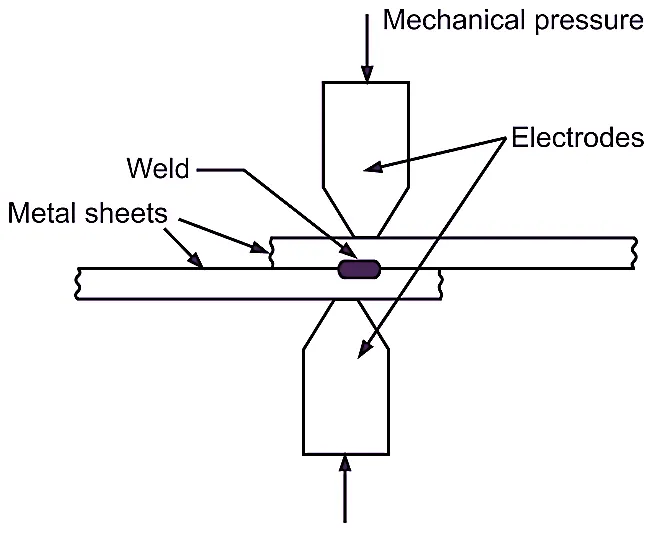
Resistance spot welding:
The process is used to joining sheet metal by apply pressure and convey the electrical current through the workpiece.
Electrode---> Copper chromium or zirconium
Heat is developed between two sheet and it is melted and it can be welded.
Resistance projection welding:
Used for mechanical fixing of autobody structure eg: Nuts
The tip will be shaped depents of parts.
Resistance seam welding:
Seam welding is the process of joining sheet metal in continuous often leak tight by directly applying opposite force with round electrode.
4.) Fusion welding:
The process involves either consumable or non consumable electrode.
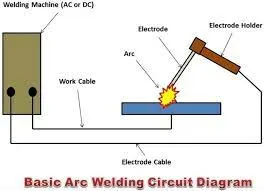
Arc produced between tip of the electrode and work piece to be welded by using AC or DC supply.
Types:
- Arc welding
- MIG welding
- TIG weldig
- Submerged arc welding
- Plasma arc welding
Arc welding:
The process of arc between the electrode and work piece, Both the electrode and work piece melt to create a weld.
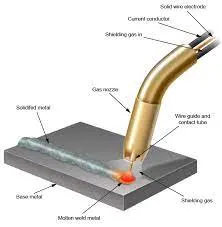
MIG welding:
The process of arc between the electrode and work piece, Both the electrode and work piece melt to create a weld.
Consumable electrode used.
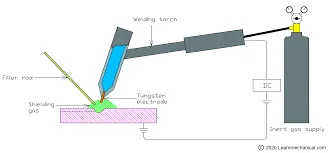
TIG welding:
The process of arc between the electrode and work piece, Both the electrode and work piece melt to create a weld.
Non Consumable electrode used.
5.) 3-2-1 Priniciple:
- The most cost effective method of part location is refered to as the 3-2-1 Principle method.
- 3--> Three locators are placed under the work piece. The three locators are usually positioned on the primary locating surface. This restricts one axial movement downward and four radial movement.
- 2--> Round pin in round hole that define location in four directions perpendicular to the plane. This restricts four axial movement.
- 1--> Round pin in a slot that defines two of the direction of the other pin. This restricts two axial movement.
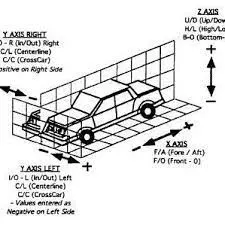
6.) Body coordinates system:
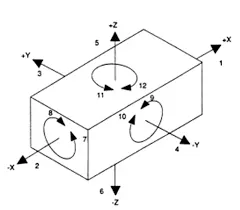
Body coordinates system has been widely used in the automotive industry for drawing a body parts.
In general BCS is also called car line and body line.
OX is define length of the car
OZ is define heigh of the car
OY is define width of the car