Week 2:- BiW Fixture Basics Challenge
- What is the process of project execution activity?
Project activities are those basically being processed or are being practiced in general projects as BIW begins. Project activities are tasks from the start to the end of the project. There are various steps involved in the project. Below fig. Show the flow chart of the project activities.
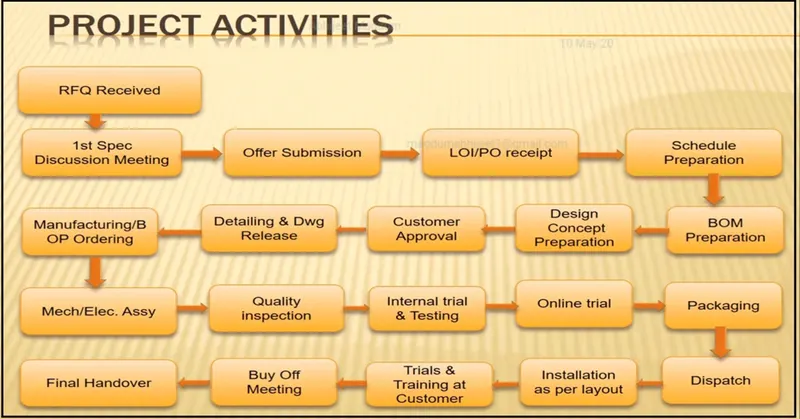
RFQ:
The BIW fixture design project begins. It starts with the basic requirements or RFQ that we receive from customers. RFQ means a request for a quotation where in customer gives his requirement specification etc. in form of some document or data to study or to work on information include such as a technical offer, commercial offer, or timeline of the project Based on that we have processing to execute the project.
1st specification discussion meeting & offer submission:
In this, the documents related to the technical offer, commercial offer, project execution, and timeline required to complete the project are prepared. The time required for 3D design, analysis of design, drawing & detailing, manufacturing, assembly & commissioning, etc. is considered. Then the cost of all operations is considered. By considering these kinds of things, the offer is prepared & submitted to the customer. Below fig. shows a document showing how a technical offer is made.
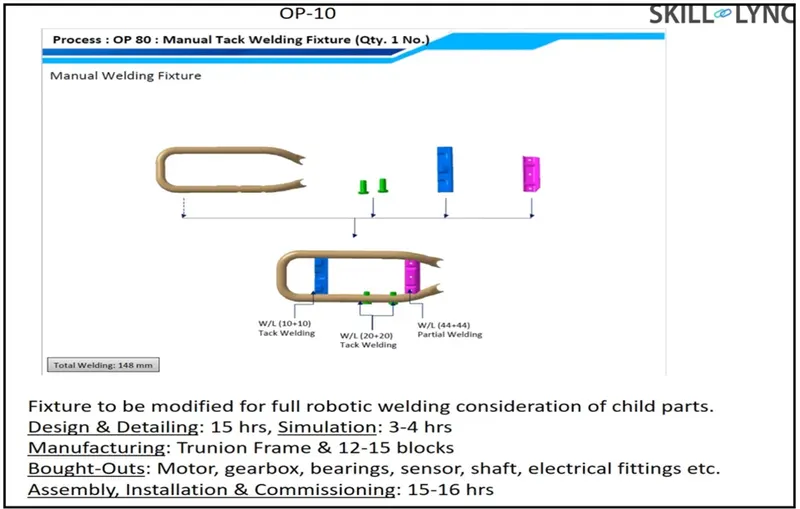
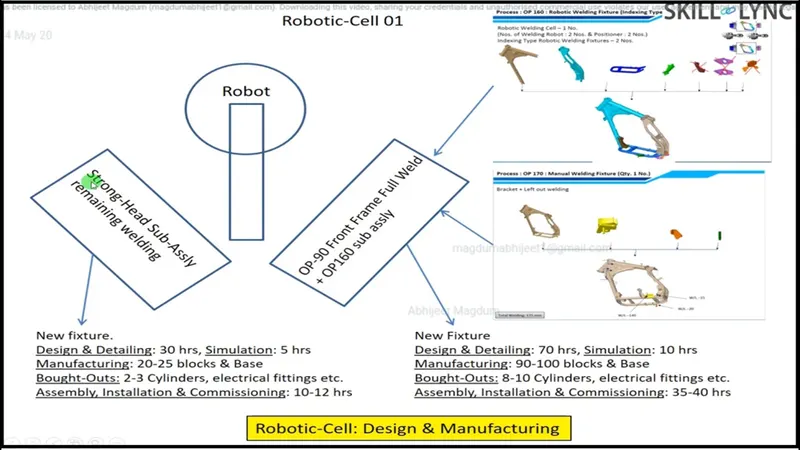
These are technical offers based on this commercial offer that will be placed.
PO/LOI: Once we submitted the offer customer will study the offer at the same time he will get offers from different suppliers & vendors. He compares these technical offers & based on cost whichever suit best for his requirement. Then he will release LOI or PO with its terms & conditions as stated earlier.
Schedule Preparation:
In the project, each activity depends on the previous activity. If the previous activity has not been completed on time it will cause a delay in the next activity date is fixed so that it can move further. Each activity has an assigned specific time i.e. when the activity is starting & when it is ending. We have some back plans so that the final date comes to a close final delivery date. There needs to be proper scheduling to be done to complete a project on time. “On-time delivery” is one of the major requirements from the customer side also customer wants commitment must be followed in respect of time.
BOM Preparation:
BOM preparation is listing down of part list which includes bought-out parts, vendor parts, and consumable items with qty. of each item. Through BOM preparation the material budget will be fixed. B/O parts include motor, gearbox, cylinder, pneumatic & hydraulic valves, etc. Also, vendor parts include all machined, fabricated parts, etc. whereas consumable includes oil, grease, glue, Loctite, etc.
Design concept preparation:
A further step is to design a concept. The concept is based on all specifications and received data from customers such as 3D data of car panel, drawing, drawing std., design std., manufacturing std. After studying all the data design concepts built.
Customer approval:
Once the design concept is ready then it will be sent to the customer for their approval. It is also known as the design approval process (DAP) or customer approval process. In that, the customer will check whether all his specification considers or not in specifications. Whether it is as per the technical offer submitted then only he approves the prepared concept. Some points will be raised by the customer. These changes have been updated to the design team by the project team. The design team will again work on it, some modifications or changes are necessary to improve the design like clamping needs to be improved or this mechanism will work fine, the sensor should be of this make. These changes are again being updated to the customer. Once he gives final approval we will move further for detailing & dwg. release.
Detailing & Dwg. release:
Detailed, all assemblies are broken down into their child parts. Parts of the assembly are segregated into std. as well as manufactured. For std. parts on the datasheet or specification sheet prepared to purchase it from the catalog. e.g. motor power, motor current rating, the torque produced, and shaft rpm which is suitable for our application. For vendor parts, all details should be provided on dwg. All dimensions of the part with tolerance, surface finish, surface treatment, hardness, and welding notes should all be mentioned in the dwg. These dwgs are checked & released for manufacturing.
Manufacturing & B/O ordering:
The manufacturing department will receive all dwg to start manufacturing of items like Mylar, blade, riser, and base frame. Also, the purchasing team will place orders for B/O parts like motor, gearbox, cylinder & valves. As the material gets ready, the QC team should inspect whether all part received is as per specification or not otherwise it will create an issue later which will waste our time
Mechanical & electrical assembly:
After QC check, parts are available for assembly. The station is the integration of all mechanical as well as electrical assemblies. The assembly team will do all the assembly as per dwg. All stations are built as per layout Then again QC team should be involved to check assembly as per the final dwg., all coordinate dimensions should be ok as per design data.
Internal trial & testing:
After the approval of QC team, Internal trials & testing started. The first step involves putting the assembly in the fixture manually to check that it is being fixed properly, locating the pin to match with the hole, clamping is ok, and loading & unloading of part is easy. The operating height is also checked, it is ergonomically correct. Then start taking trials on fixtures for welding feasibility and gun approachability in fixtures. Then go for an online trial.
Online training:
After a successful trial, the next step is online training. Online training has two modes manual & automated. An online trial system is run through the control panel. All sensors, actuators, motor currents & temperatures, noise, all alarms, and safety should also be tested. All processes must be executed as per sequence and also cycle time met. An online training system that runs for a certain cycle & actual production is taken to ensure the system runs successfully.
Packaging:
After the trial gets successful, the customer gives the approval to the dispatch system. To dispatch the whole system needs to disassemble station-wise & pack properly. Delicate material should be packed properly otherwise there is a chance of damage aesthetically or functionally during transportation. During packaging labeling, special handling instructions should be pasted on particular parts to convey the message of being taken care of during handling & transportation.
Dispatch:
All materials are transported at the customer site through trucks, containers, and ships or by air.
Installations:
All system is assembled & installed at the customer’s end as per the layout approved initially in DAP. All stations, robots, and conveyors are mounted as per the distance specified in the layout. The robot arm should be reachable at the station, pick & drop point. It shouldn’t foul with other equipment. Also, some adjustments should be provided for leveling purposes at the robot conveyor base and station base frames like leveling studs to align with other equipment. The layout is always specified at the time of the initial design stage & it has to be approved by the customer.
Trial & training at customer end:
Once the installation is done the trial starts at the customer's end. So there will be a production trial and an online trial. Production trials are necessary because at the time of designing the fixture, it was also committed to no. of units that will be manufactured from that fixture as well as whether it is meeting quality, benchmark, or not. Also, regarding the technical offer... we are committed that there will be 100 units per 8hrs shift that will be manufactured from that fixture with weld quality. So during the production trial, fixture capability will be ensured. Once this goal is achieved then there will be training for operators, staff members, and engineers to help them understand how the process works.
Buy-off meeting:
Once the training is completed, there will be a buy-off meeting between the customer & project team with a discussion on if their other things need to be incorporated, or if anything is missing that is described in LOI/PO or offer submission. The customer will raise a point or sometimes the customer wants modifications that will lead to extra quotations and extra costing according to when work is done as per buy of meeting.
Final handover:
Once all points raised by the customer are closed then all will go for the final handover. All data, technical manuals, and soft and hard documents will be submitted to the customer. These are the main project activities.
- What are the types of joining processes?
There are many joining processes used in BIW like welding and gluing.
The durability and performance of any structure largely depend on the quality & design of components joints. The whole structure can’t be made in one piece. Two fundamental options for joining material & components.
- Metallurgical joining
- Mechanical joining.
- Metallurgical joining: In welding, two or more parts are heated & melted or forced together, causing the joined parts to function as one. In some welding methods, filler material is added to make the merging of materials easier.
Welding:
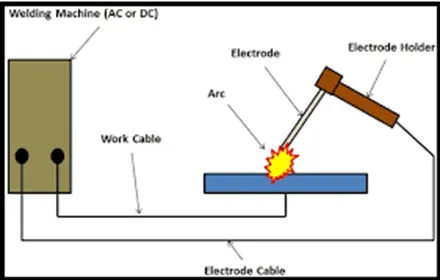
Welding is the process of permanently joining material welding joins different metals/ alloys with a number of processes in which heat is supplied either electrically or by means of a torch. Welding is done by the application of heat or both heat & pressure. Pressure may be employed, but this is not in many processes essential. The welding process involves applying heat to the workpiece. The heat applied should be such that the workpiece should melt, i.e. the temperature at which welding is done should be more than the melting point of the workpiece to be welded. Welding is a fabrication or sculptural process that joins materials, usually metals or thermoplastics, by using high heat to melt the parts together and allowing them to cool, causing fusion. Welding is distinct from lower-temperature metal-joining techniques such as brazing and soldering, which do not melt the base metal. In addition to melting the base metal, a filler material is typically added to the joint to form a pool of molten material (the weld pool) that cools to form a joint that, based on weld configuration (butt, full penetration, fillet, etc.), can be stronger than the base material (parent metal). Pressure may also be used in conjunction with heat or by itself to produce a weld. Welding also requires a form of shield to protect the filler metals or melted metals from being contaminated or oxidized. Many different energy sources can be used for welding, including a gas flame (chemical), an electric arc (electrical), a laser, an electron beam, friction, and ultrasound. While often an industrial process, welding may be performed in many different environments, including in open air, underwater, and outer space. Welding is a hazardous undertaking and precautions are required to avoid burns, electric shock, vision damage, inhalation of poisonous gases and fumes, and exposure to intense ultraviolet radiation. Below fig. shows the principles of welding.
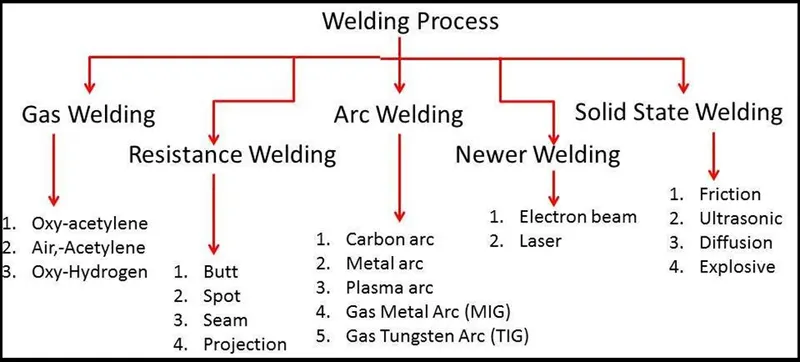
There are many different types of welding operations, such as the various arc welding, resistance welding, and oxyfuel gas welding methods. Below fig. illustrate different types of the welding process.
Brazing:
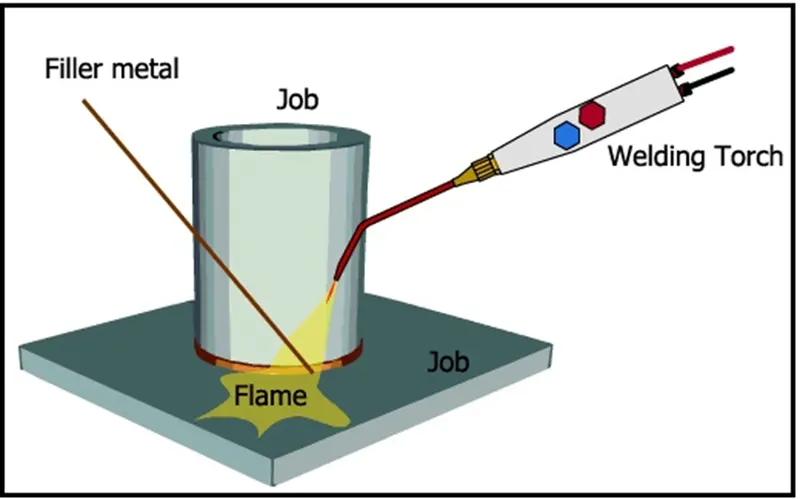
During the brazing process, a filler metal is melted & distributed between multiple solid metal components after they have been heated to the proper temperature. The filler metal must have been a melting point that is above 840. Brazing is a metal-joining process in which two or more metal items are joined together by melting and flowing a filler metal into the joint, the filler metal having a lower melting point than the adjoining metal.
Brazing differs from welding in that it does not involve melting the work pieces and from soldering in using higher temperatures for a similar process, while also requiring much more closely fitted parts than when soldering. The filler metal flows into the gap between close-fitting parts by capillary action. The filler metal is brought slightly above its melting (liquidus) temperature while protected by a suitable atmosphere, usually a flux. It then flows over the base metal (in a process known as wetting) and is then cooled to join the workpieces together. A major advantage of brazing is the ability to join the same or different metals with considerable strength. The figure below shows the brazing process.
Soldering:
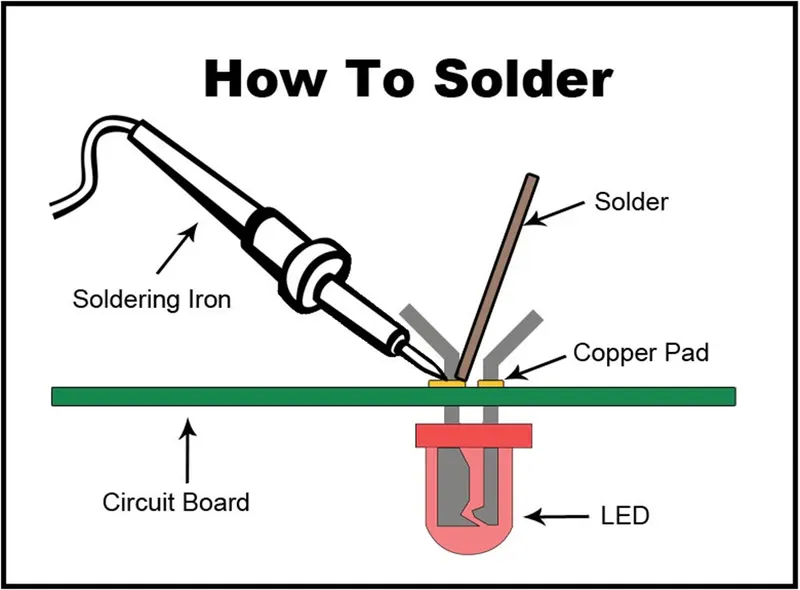
Soldering is a process in which two or more items are joined together by melting and putting a filler metal (solder) into the joint, the filler metal having a lower melting point than the adjoining metal. Unlike welding, soldering does not involve melting the work pieces. In brazing, the workpiece metal also does not melt, but the filler metal is one that melts at a higher temperature than in soldering. In the past, nearly all soldiers contained lead, but environmental and health concerns have increasingly dictated the use of lead-free alloys for electronics and plumbing purposes. Soldering is used in plumbing, electronics, and metalwork from flashing to jewelry and musical instruments. The figure below is shown as a piece of information.
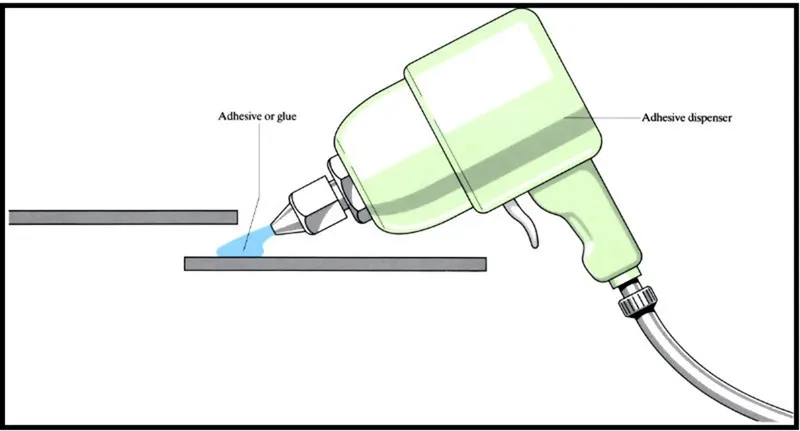
Adhesive bonding-
Adhesive bonding (also referred to as gluing or glue bonding) describes a wafer bonding technique by applying an intermediate layer to connect substrates of different types of materials. The connections produced can be soluble or insoluble. The commercially available adhesive can be organic or inorganic and is deposited on one or both substrate surfaces. Adhesives, especially the well-established SU-8, and benzocyclobutene (BCB), are specialized for MEMS or electronic component production. The procedure enables bonding temperatures from 1000 °C down to room temperature. The most important process parameters for achieving a high bonding strength are adhesive material, coating thickness, bonding temperature, processing time, chamber pressure, and tool pressure.
Adhesive bonding has the advantage of relatively low bonding temperature as well as the absence of electric voltage and current. Based on the fact that the wafers are not in direct contact, this procedure enables the use of different substrates, e.g. silicon, glass, metals and other semiconductor materials. A drawback is that small structures become wider during patterning which hampers the production of an accurate intermediate layer with tight dimension control. Further, the possibility of corrosion due to out-gassed products, thermal instability, and penetration of moisture limits the reliability of the bonding process. Another disadvantage is the missing possibility of hermetically sealed encapsulation due to the higher permeability of gas and water molecules while using organic adhesives. Below figure shown for additional information.
Diffusion bonding:
Diffusion bonding or diffusion welding is a solid-state welding technique used in metalworking, capable of joining similar and dissimilar metals. It operates on the principle of solid-state diffusion, wherein the atoms of two solid, metallic surfaces intersperse themselves over time. This is typically accomplished at an elevated temperature, approximately 50-70% of the absolute melting temperature of the materials. Diffusion bonding is usually implemented by applying high pressure, in conjunction with necessarily high temperature, to the materials to be welded; the technique is most commonly used to weld "sandwiches" of alternating layers of thin metal foil, and metal wires or filaments. Currently, the diffusion bonding method is widely used in the joining of high-strength and refractory metals within the aerospace and nuclear industries.
Mechanical joining:
Mechanical joining is a process for joining parts through clamping or fastening using screws, bolts, or rivets. Advantages of mechanical joining include versatility, ease of use, and the option to dismantle the product in cases where regular maintenance requires it. The ability to join dissimilar materials is another benefit. A drawback of using mechanical joining is the lack of a continuous connection between parts because the joint is achieved through discrete points. Also, holes created for joining are vulnerable to fractures and corrosion.
Mechanical joining – also called joining by forming – has become interesting for the automotive industry due to the request to reduce fuel consumption and thereby emissions. In order to reduce weight on the car body, the usage of lightweight materials in the body-in-white application has increased. This includes aluminum, high-strength steel alloys, polymers, and composites. Here the different types of mechanical joining become important. All mechanical joining methods are cold-forming techniques. One general benefit of all mechanical joining methods is the mobility of the material after joining. At the same time, mechanical joining offers impressive strength.
a) Mechanical fastening:
The joining of material combinations which cannot be easily welded such as pre-painted steel or very dissimilar metal. Ex. AI application in autobody makes use of mechanical fastening to overcome the poor inherent weldability of AI.
The joining of materials in applications where high fatigue life is critical compared to static strength.
The joining of materials where high tool life is of relative importance
e.g. screws, bolts, etc
- b) Self-piercing riveting:
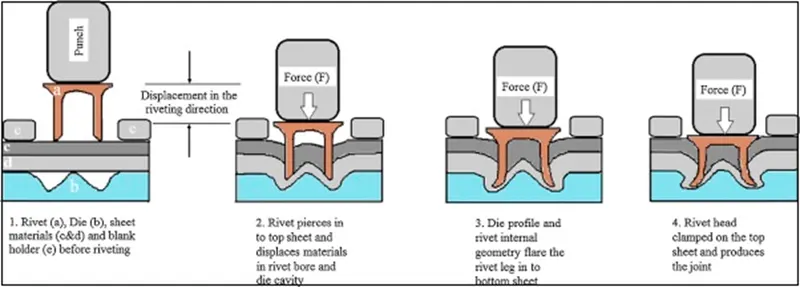
Self-piercing riveting is high-speed mechanical fastening for point-joining sheet material, typically steel & aluminum alloys. It is a single-step technique generally using a semi-tubular rivet to clinch the sheet in the mechanical joint. There is also a process variant that utilizes solid rivets.
The name suggests that pre-drilled holes are not required, allowing the joint to be made rapidly in one operation. The process cycle is shown in the cross-section below.
Hemming & seaming process:
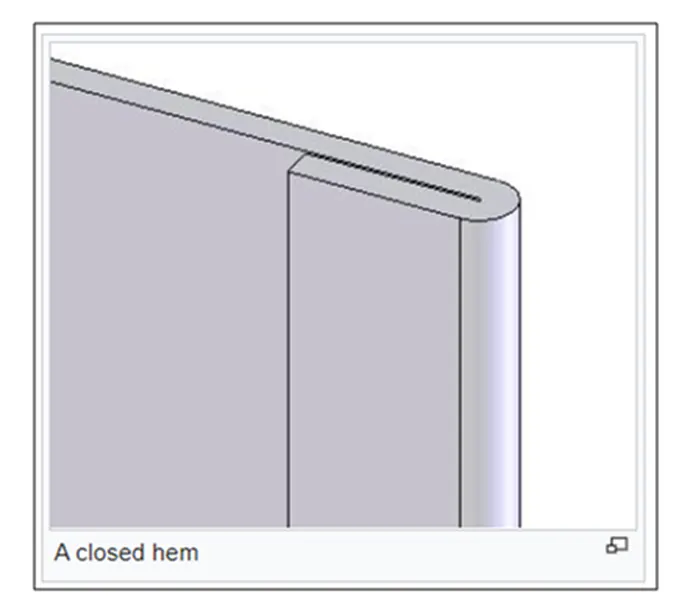
Hemming & seaming are two similar metalworking processes in which a sheet metal edge is rolled over onto itself. Hemming is a process in which the edge is rolled flush to itself, while the seam joins the edges of two materials. Hems are commonly used to reinforce an edge, hide burrs and rough edges, and improve appearance. Seams are commonly used in the food industry on canned goods, on amusement park cars, in metal roofing (with a roof seamer), and in the automotive industry. The process for both hemming and seaming is the same, except that the tonnage requirement is greater for seaming. The process starts by bending the edge to an acute angle. A flattening die is then used to flatten the hem. The below figure illustrates hem formation.
What is Resistance Welding & its application in the automotive sector?
- Resistance welding is a technology widely used in the manufacturing industry for joining sheet metal & components.
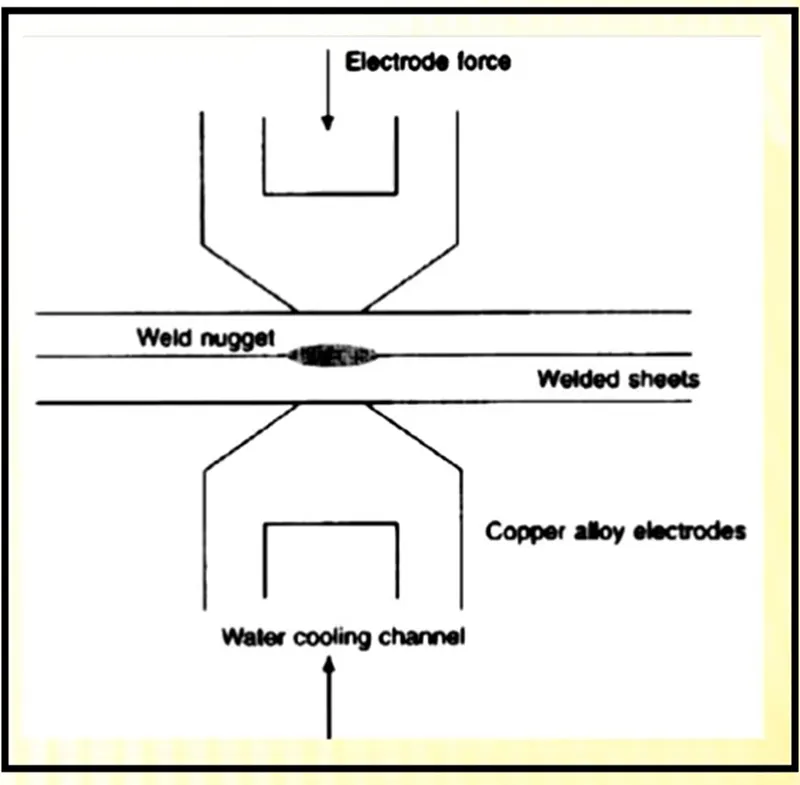
- The weld is made by conducting a strong current through the metal combination to heat up & finally melt metal at localized points predetermined by the design of electrodes and or the workpiece to be welded.
- A force is always applied before, during & after the application of currents to confine the contact area at the weld interface & in some workpieces to forge the workpiece. Below fig. shows resistance welding techniques.
Types of resistance welding:
- Resistance spot welding
- Resistance seam welding
- Resistance projection welding.
1). Resistance spot welding-
Resistance spot welding is widely used in BIW joining processes. The process is used for joining sheet materials & uses shaped copper chromium or zirconium alloy electrode to apply pressure & convey electrical current through the workpiece. Heat is developed mainly at the interface between two sheets, eventually causing the material to be welded to melt, forming a molten pool & weld nugget. The molten pool is contained by the pressure applied by the electrode tip & surrounding solid metal. When the circuit is completed current will flow from that panel or sheet metal which will generate the amount of heat that is sufficient enough to melt that will be melted & get welded together. The molten pool should not be moved outside of that zone to ensure that proper pressure is applied through the electrode tip & surrounding sheet metal. Forcing a large current through the spot will melt the metal and form the weld. The attractive feature of spot welding is that much energy can be delivered to the spot in a very short time (approximately 10–100 milliseconds). This permits the welding to occur without excessive heating of the remainder of the sheet. Strength & durability largely depends on the quality of RSW. The figure below illustrates the principle of resistance welding.
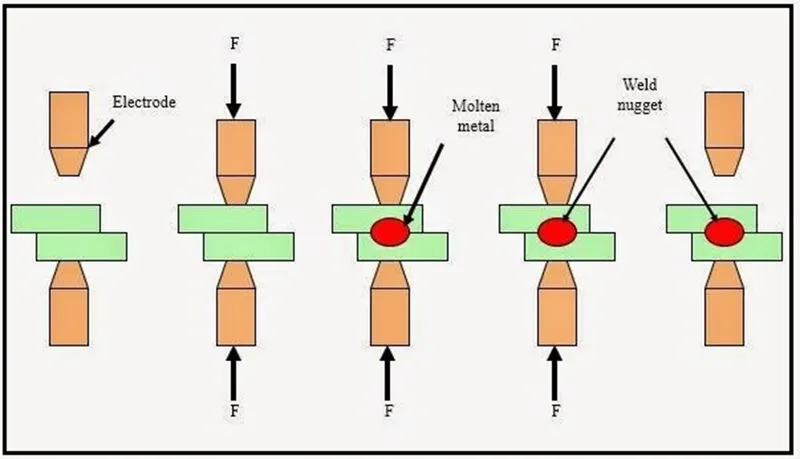
The following are the advantages of resistance spot welding.
Short weld time & hence high weld speed
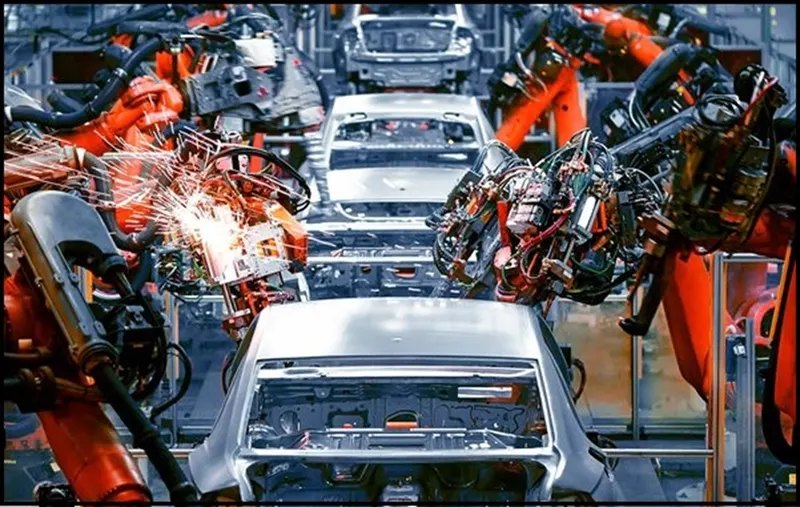
Highly adaptable to automation & robotic technique. The below figure show robot used in the automotive industry for spot welding. A typical BIW contains 500 welds. RSW is automated and used in the form of robotic spot welding in automotive industries to weld sheet metals to form car bodies. The figure below illustrates a typical application of spot welding using robots.
Resistance seam welding:
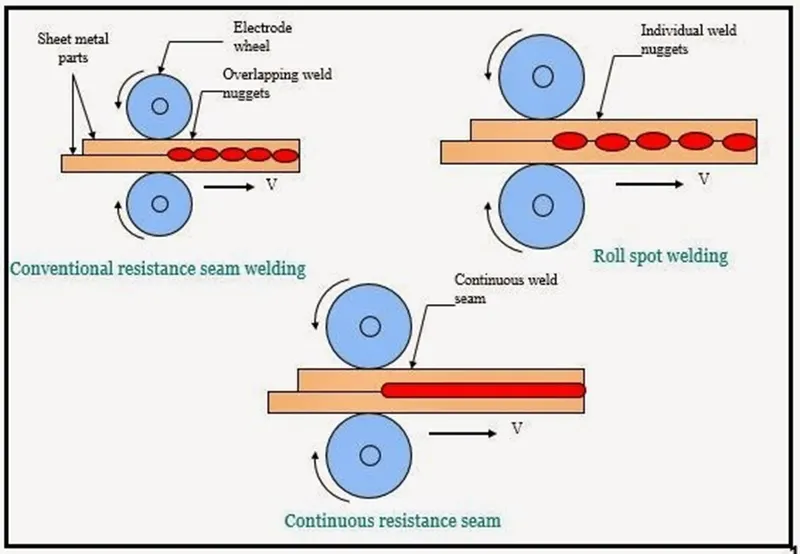
Resistance seam welding is a welding process for joining metal sheets in continuous, often leak-tight, seam joints by directly applying opposing forces with electrodes consisting of the rotary wheel. It differs from flash welding in that flash welding typically welds the entire joint at once and seam welding forms the weld progressively, starting at one end. The current & the heat generation is localized by peripheral shapes of the electrode wheel Seam welding is mostly applied in the manufacturing of containers radiators & heat exchangers etc. Resistance seam welding is used where leakage-proof continuous welding is required. Like spot welding, seam welding relies on two electrodes, usually made from copper, to apply pressure and current. The electrodes are often disc-shaped and rotate as the material passes between them. This allows the electrodes to stay in constant contact with the material to make long continuous welds. The electrodes may also move or assist in the movement of the material. Seam welding produces an extremely durable weld because the joint is forged due to the heat and pressure applied. A properly welded joint formed by resistance welding can easily be stronger than the material from which it is formed. A common use of seam welding is during the manufacture of round or rectangular steel tubing. Seam welding has been used to manufacture steel beverage cans but is no longer used for this as modern beverage cans are seamless aluminum. In automobile industries, this welding process is used to produce leak-proof fuel tanks.
Resistance projection welding:
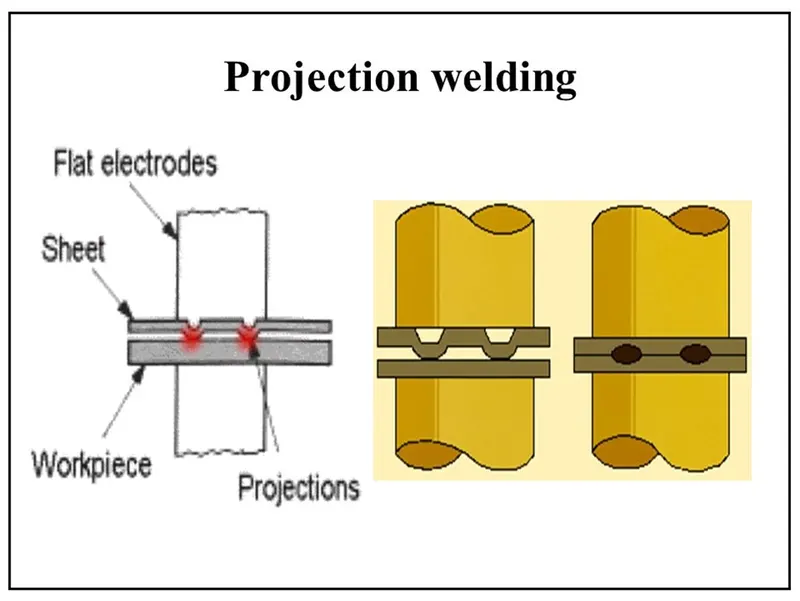
Projection welding is the process of joining metal components or sheets with embossment by directly applying opposing forces with electrodes specially designed to fit the shape of workpieces. The current & heat generation is localized by the shape of workpieces either with their natural shape or with specially designed projection. Large deformation or collapse will occur in the projection part of the workpiece. This process has the benefit of forcing the welds to occur in very specific and tiny locations and minimizing the dissipation of heat to the rest of the metal sheets.
It is used for mechanical fixing of auto body structures e.g. to weld nuts. In the BIW body, there will be many welded nuts, studs, and bolts that need to be welded on the sheet. It will use further stages of the fastening process. So to weld these things we use processes like resistance welding. The concept & mechanism is the same as using two electrodes. The current will flow, pressure will be applied, and metal will melt & get welded together. Spot welding will have a rounded tip at the end of the electrode. For projection welding, the tip will be the same as per the part as per profile.
What are fusion welding & types of fusion welding with its application in the automotive sector?
In fusion-welding processes, heat is applied to melt the base metals. In many fusion welding processes, a filler metal is added to the molten pool during welding to facilitate the process and provide strength to the welded joint. When no filler metal is used, that fusion welding operation is referred to as an autogenous weld. Fusion welding is unique, however, because of its ability to “fuse” the respective objects. Assuming the objects are made of the same or similar materials, the heat produced by a welding rig will melt their surfaces, thereby allowing the objects to fuse together. Fusion welding is categorized according to the source of heat for example electric arc, electric resistance, gas, and high energy.
Arc Welding:
The most popular type of fusion welding is arc welding. The process involves either a consumable or non-consumable electrode rod or wire. Arc welding lives up to its namesake by relying on an electric arc to join two or more objects. An arc is produced between the tip of the electrode & workpiece to be welded by an AC or a DC power supply. With electric arcs measuring up to 6,000 degrees Fahrenheit, this fusion welding process is highly capable of melting even the toughest metals. Furthermore, arc welding can be performed underwater, making it an ideal solution for offshore welding projects. This process can be categorized into two different types; consumable and non-consumable electrode methods. Below figure shows.
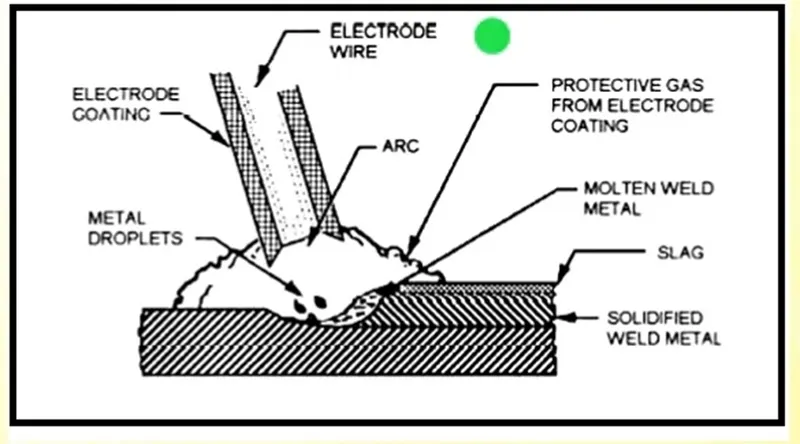
Manual metal arc welding or Shielded Metal Arc Welding (SMAW):
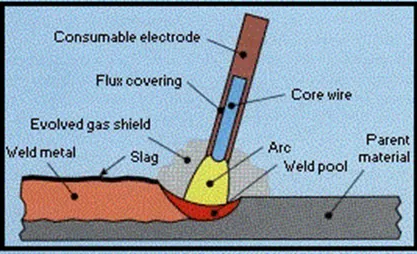
Also known as manual metal arc welding (MMA or MMAW), flux-shielded arc welding or stick welding is a process where the arc is struck between the metal rod (electrode flux-coated) and the workpiece, both the rod and workpiece surface melt to form a weld pool. Simultaneous melting of the flux coating on the rod will form gas and slag, which protects the weld pool from the surrounding atmosphere. This is a versatile process ideal for joining ferrous and non-ferrous materials with a range of material thicknesses in all positions. Below figure shows.
Gas-shielded metal arc welding or metal inert gas welding or MIG:
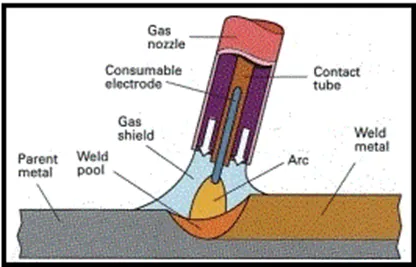
Metal inert gas (MIG) is an arc welding technique in which a consumable electrode is used to weld two or more workpieces. MIG welding is the most common arc welding process, in which arc forms between consumable wire electrodes & workpieces leading them to melt & join. Both use a shielding gas to protect the weld from airborne contaminants or oxidation in the case of MIG welding. The process can be automatic or semi-automatic. A constant voltage, direct current power is most commonly used with GMAW, but a constant current system, as well as AC, can be used. There are four primary methods of metal transfer in GMAW, called globular, short-circuiting spray, each of which has distant properties & corresponding advantages & limitations. MIG welding makes use of the following components,
- Consumable electrode
- Inert gas supply
- Welding head
- AC and DC power supplies.
Gas-shielded tungsten arc welding or TIG:
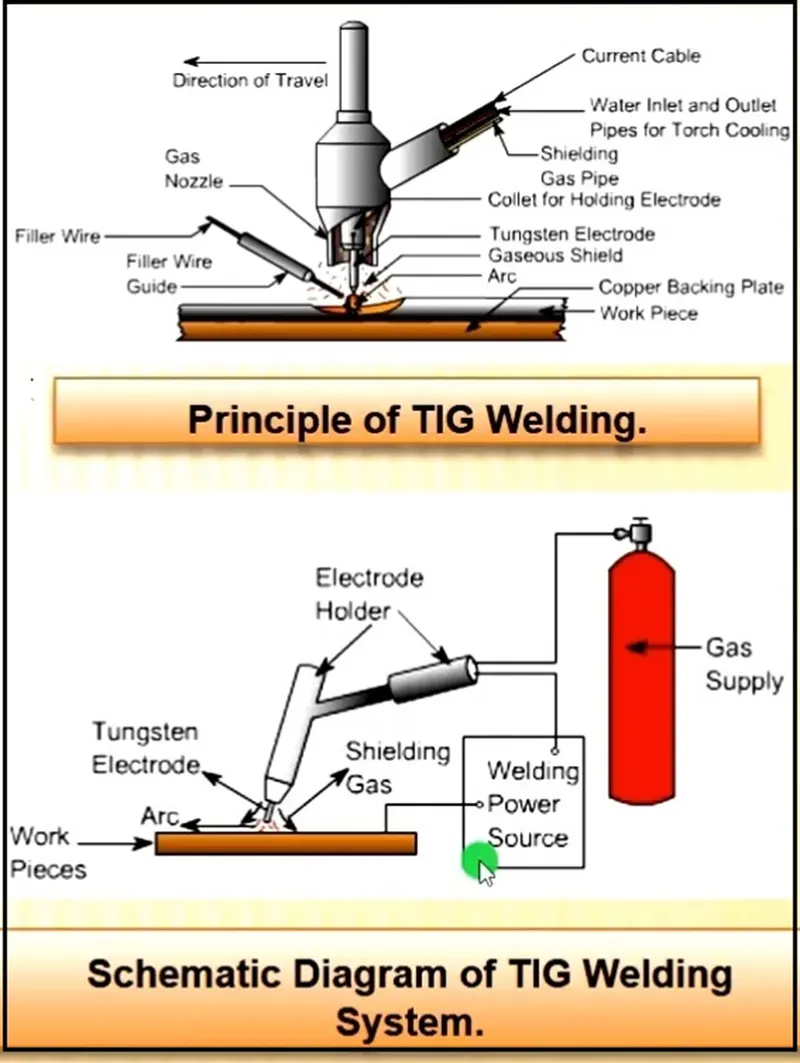
Tungsten inert gas welding, also known as gas tungsten arc welding (GTAW), is an arc welding method that uses a non-consumable tungsten electrode to weld two or more workpieces. An inert shielding gas is used to protect from oxidation or other atmospheric contamination. The process can be used autogenously on thin parts but will require the addition of a wire, rod or consumable to be added for thicker parts. A constant current welding power supply produces electrical energy, which is conducted across the arc through a column of highly ionized gas & metal vapors known as plasma. It is very much similar to metal inert gas welding (MIG). The following components are necessary to perform tungsten inert gas welding.
- Power supply
- Non-consumable tungsten electrode
- Inert gas supply
- Filler rod (depending on the nature of the workpiece)
- Welding heads.
Plasma arc welding:
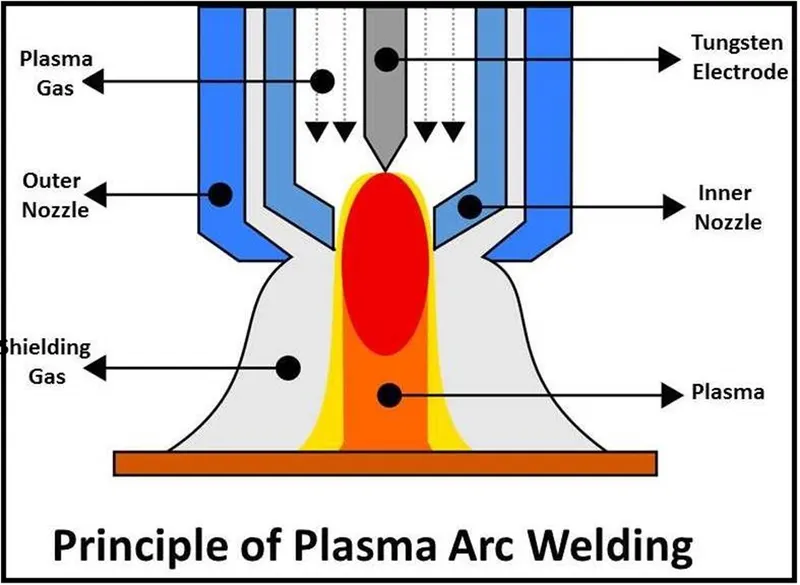
Plasma arc welding (PAW) is similar to GTAW or gas tungsten welding. In this kind of welding process, the arc will generate among the work part as well as the tungsten electrode. The major dissimilarity between plasma arc welding and gas tungsten welding is that the electrode is located within the torch of Plasma arc welding. The gas can be heated at the temperature of 30000°F & change into plasma to attack the welding region. The figure below shows the working principles of plasma arc welding.
Submerged Arc Welding:
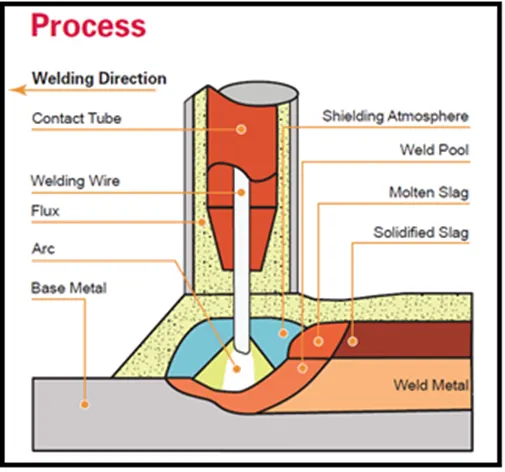
Submerged arc welding (SAW) can be extensively utilized within an automatic welding method. In this kind of welding process, an electrode is completely submerged by the granular coating of flux, and this flux can be an electric conductor which will not oppose the electric supply. The solid coating of flux stops the melted metal to ultra-violate radiation and the atmosphere. Below fig. show.
Automotive application of arc welding technology:
Arc welding is used to weld chassis parts in the automotive industry.
Arc welding is used to weld body parts in the automotive industry. Low heat input welding of thin steel sheets prevents burn-through due to excessive heat input is important in the welding of car body parts of thin sheets. For this reason, a thin welding wire with a diameter of 0.9 mm, enables welding at low currents & low heat input welding power source.
TIG welding is used to join thin stainless steel parts & various piping parts in the automobile industry. TIG welding can work on both AC and DC power sources. One of the greatest strengths of TIG welding is that it can be used for welding non-ferrous metals like aluminum, copper, magnesium, copper, nickel, titanium, etc.
Rebuilding: MIG welding is used for repairing work in the automobile industry. To repair it, especially to dismantle & reassemble it with new parts. Example: to rebuild an old car. When it comes to fixing broken parts in the field, there are three steps to master: cutting & removal of the failed component, preparation of the new joint/ part, and welding & cleanup. Worn parts can be repaired using MIG welding in a variety of coatings (stainless steel, bronze, nickel, aluminium, or hard surfacing) & in a range of hardness, for a fraction of the cost of purchasing a new part.
What is the 3-2-1 principle?
Degrees of freedom: The degree of freedom is defined as the capability of a body to move. Consider a rectangular box, in space the box is capable of moving in twelve different directions (six rotational & six axial).
6 translational degrees of freedom: +X, -X, +Y, -Y, +Z, -Z.
6 rotational degrees of freedom:
- Clockwise around the X axis (CROT-X).
- Anticlockwise around the X axis (ACROT-X).
- Clockwise around the Y axis (CROT-Y).
- Anticlockwise around the Y axis (ACROT-Y).
- Clockwise around the Z axis (CROT-Z).
- Anticlockwise around the Z axis (ACROT-Z).
Each direction of movement is counted as one degree of freedom. i.e., a body in space has twelve degrees of freedom.
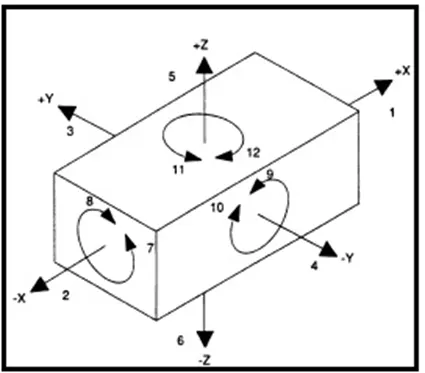
The above figure shows a body in space & its possible direction of movement. The body can move in two directions along each axis of three mutually perpendicular axes; also can rotate about this axis either clockwise or anticlockwise. There are twelve degrees of freedom for the body in space.
In the machining process, in order to attain specific results, the degrees of freedom are constrained by using work-holding devices, jig & fixture & locating devices. There must be a definite relationship between the cutting tool & surface of the workpiece in order to perform the accurate cutting operation. To achieve high precision in machining, the workpiece must be located accurately; it is called locating the workpiece. The location of the components is significant to the design of the jig & fixture so that it influences the accuracy of the final product. The locating device is designed so that each successive workpiece loaded must occupy the same position in work handling devices.
Locating: the positional & dimensional relationship between the workpiece & cutting tool.
Locator: the device to establish & maintain the position of the workpiece in work holders such as jig & fixture to ensure repeatability of the work holder.
The best & most effective method of part location is the 3-2-1 principle. Holding fixtures used in assembly operations often follow a 3-2-1 locating scheme to position parts. Under this scheme, three locators position a part in a primary plane or direction (e.g., high/low). Two locators then position the part in a second direction (e.g., in/out), leaving one locator for the tertiary direction (e.g., fore/aft). This approach fixes the part in 3-dimensional space and satisfies the six degrees of freedom constraint.
(3) minimum plane: Three locator blocks to establish the part plane. Three locators or supports are placed under the workpiece. Three locators are usually positioned on the primary locating surface. This restricts one axial movement downward, & 4 radial movements. Together, the three locators restrict five degrees of freedom.
(2) Round locating pin in a round hole that defines the location in four directions (4 ways) perpendicular to the plane previously established. This restricts four axial movements.
(1) Round locating the pin in the slot that defines two of the other pins (2-way). This restricts two axial movements.
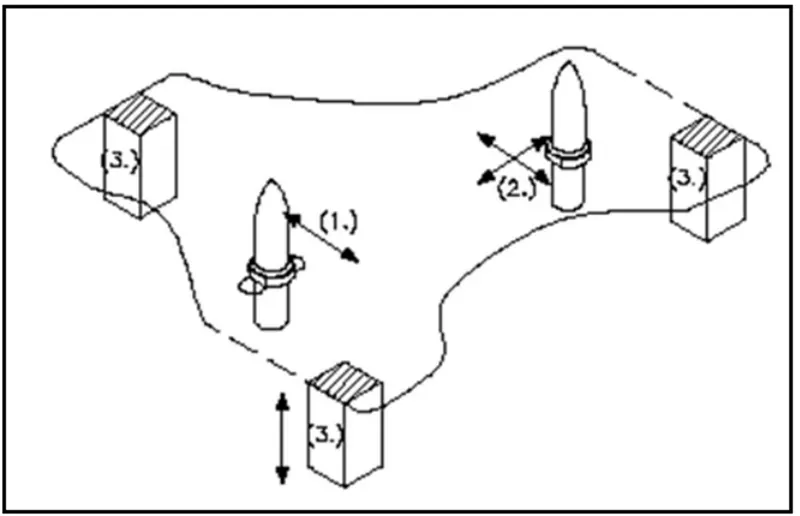
A better way of understanding the 3-2-1 principle considers 12 degrees as 6 degrees of freedom. It includes clockwise & anticlockwise as one rotation. Movement in +ve & -ve direction as one translation motion. So we have three translation motions in the x, y, and z axis & three rotational motions about the x, y, and z-axis.
In this, (3) means restricting three degrees of freedom as a translation motion in the z-axis i.e. upward & downward, two rotational motions about the x & y axis.
Secondly, (2) means restricting two degrees of freedom. Translating motion in x (i.e. +ve or –ve) & y direction i.e. (+ve or –ve) & (1) means restricting one degree of freedom i.e. rotational motion about the z-axis clockwise or anticlockwise. So the car panel or body cannot move in any direction with or without the application of external force so properly fixed in the fixture. This is the basic concept of designing fixtures.
Define Body coordination system.
BODY COORDINATE SYSTEM (Part Locating System)
The body coordinate system has been widely used in the automotive industry for drawing body parts, and product & process design. A coordinate system is a reference system consisting of a set of points, lines & surfaces, used to define the positions of points in space in either two or three dimensions. In general, BCS is also called a car line & body line.
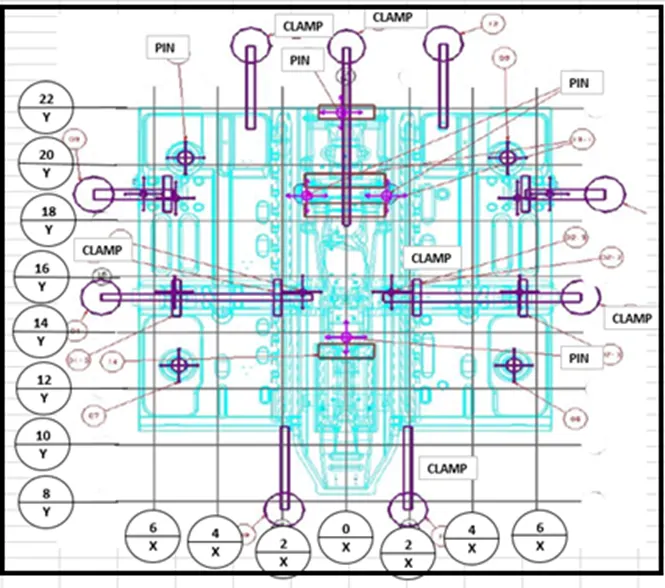
Car lines are the (grid lines) shown on the fixture, which virtually represent the same location in BIW. The entire car line on the fixture displays the coordinates at the corner for reference. With these lines, one can easily relate to the location in BIW.
Sometimes the single coordinate hole is given in a fixture that also represents the car line coordinates, from which the reference point fixture is made & can be inspected. Body coordinates are mentioned near the hole. The figure below shows the car line on the fixture.
Automotive sheet metal components are designed in CAD (Computer-aided Design) software e.g. CATIAv4-v5, UG, ProE, Ideas,
In any CAD tool, there is a default axis system of X, Y, and Z.
Let us consider if every designer starts the design of the BIW Door Assembly part with a default axis system, then it will be difficult to assemble or position the part with respect to each other.
To avoid this issue, BIW car panels are designed with reference to car axis means at their
The original location of the final car was built.
The reference axis system of the software is used for the design of the various features of the parts (e.g. hole, fillet, threads) to correlate the position of all the automotive components during the final assembly the axis system of the vehicle is used. Most of the time the vehicle axis system and software axis system are the same. e.g. In most European OEMs, The X-axis represents the length of the vehicle Y-axis represents the width of the vehicle Z-axis presents the height of the vehicle. Y-axis is considered to be located at the front axle. All BIW welding fixtures are designed with reference to the car line
These datum schemes provide a reference system for all part surfaces and features using body coordinates. The figure below illustrates a typical body coordinate system. This system replaces the traditional X, Y, and Z directional designations with fore/aft (X), in/out (Y), and up/down or high/low (Z). The 0,0,0 point of the car is the front, lower, and center positions.
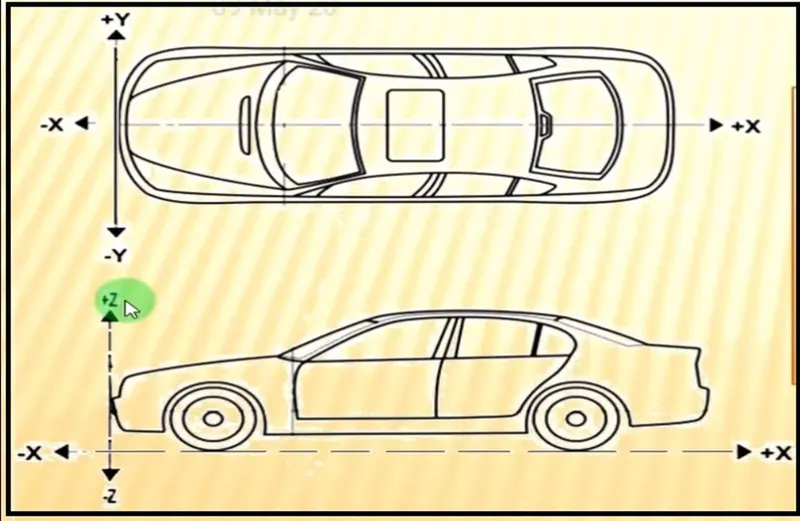
VEHICLE ORIENTATION: All vehicle product drawings are identified numerically relative to the three-vehicle planes described and shown below.
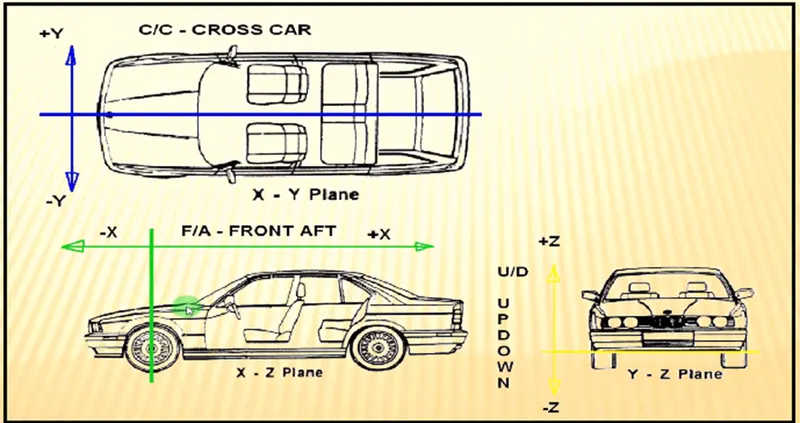
X= longitudinal direction (fore & after-F/A) or (Front O line-FOL).
Y= transverse direction (Cross car-C/C) or (Centre O line-COL).
Z= Vertical direction (Up & down- U/D) or (Bottom O Line-BOL).
The origin of the body coordinate system (OX) is defined at the front center of a vehicle. It indicates that the length of the car & the coordinate system (OZ) below its underbody indicates the height of the car & the coordinate system (OY) whose starting point is the center of the car's body indicates the width of the car.
Maintaining X, Y & Z coordinates in the fixture is a very important factor.
We should try that the coordinates of locating & clamping points should not be in three decimal (e.g. X=100.124, Y=245.127, Z=450.458)
They should be in whole nos or max up to 1 decimal. Once these coordinates are maintained automatically, the BIW base structure is maintained.
Elaborate Body plane system & its essentials.
Body planes are the reference planes in an automotive car. These planes are used to define the GD & T of all car parts in the automotive domain.
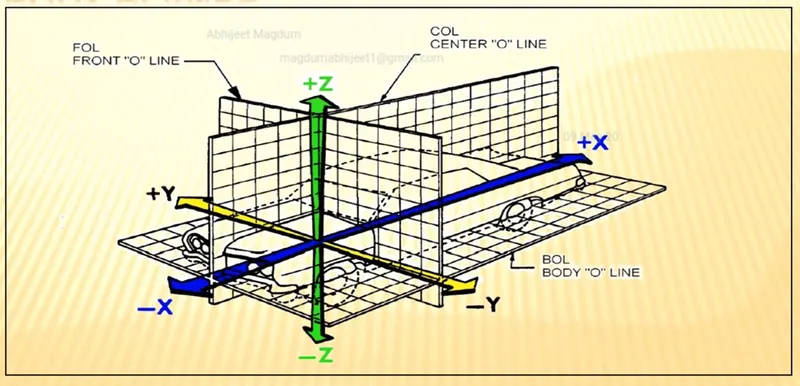
Body planes are three mutually perpendicular imaginary planes. These are generally considered to be present at the driver position or sometimes at the engine location or at the front end of the car depending on the customer.
The measurements from the body planes to the parts are called body line dimensions.
These body planes are called as
FOL Front “O” line.
COL Centre “O” line
BOL Body “O’ line
The measurement along FOL or X-axis is called F/A Front aft.
The measurement along COL and Y-axis is called a C/C Cross car.
The measurement along BOL or Z-axis is called U/DUP down.
The below figure origin is somewhere below the drive sheet as it depends on or changes from customer to customer. But the axis system is commonly the same.
Bodyline dimensions are essential for the reasons stated below,
- It defines the exact position of each product in the vehicle w.r.t.a fixed origin.
- It ensures flawless design for assembly.
- While designing lines, all the designs are carried out relative to the bodyline, viz, fixture, turn table, etc.
- It assists in the easy location of different parts of a vehicle.
- It aims to create a standardized system.
- They assist in quality checks.
These are the basic essential things that body line dimensions would help in BIW. It could help in designing lines like welding lines, assembly lines, or car bodies through fixtures & turntables,s, etc. This will help in designing all the tools. Particular assemblies or parts are designed w.r.t body lines or an axis system or car line also helps in quality while doing CMM of that system. CMM is basically done with the help of coordination. It has a related a particular fixture with that car part because the dimensions and coordinates of the hole & pin should match so it will help in quality check also. We only give coordinates that belong to that hole, both coordinates should match. This matching means the quality is approved. The figure below shows some examples.
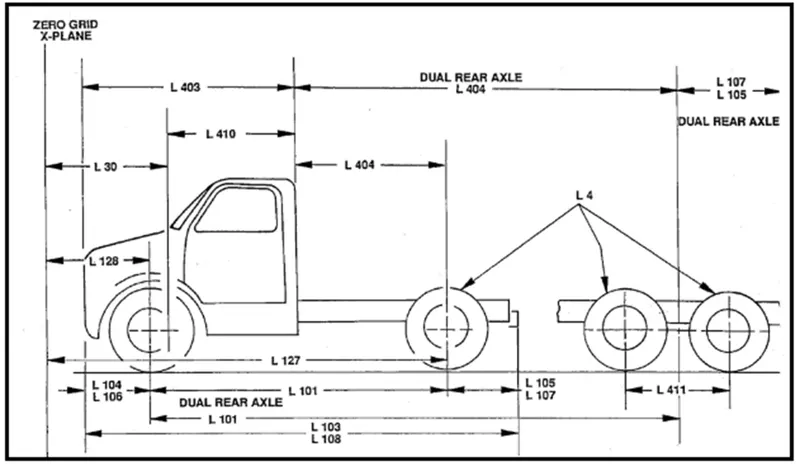
Fig shows the use of the X plane to define the length of the car.
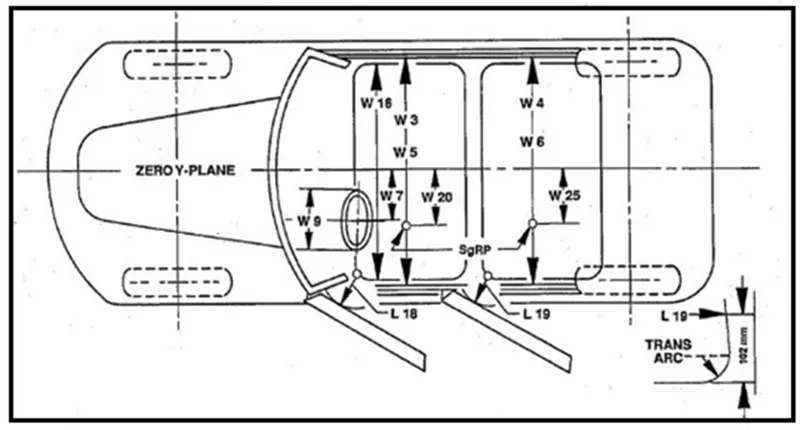
The below figure shows the use of the Y plane to define the width of the car.
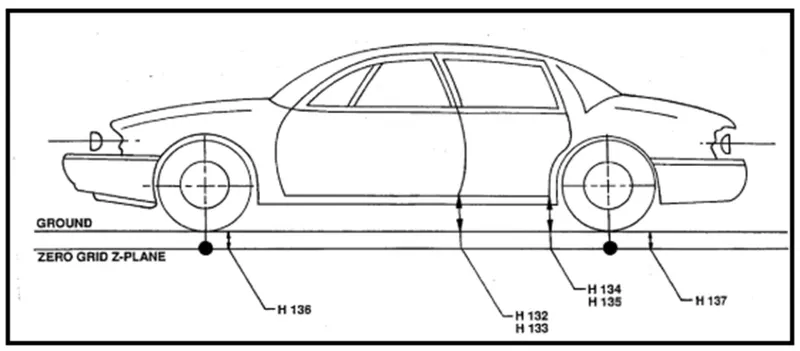
The figure below shows the use of the Z plane to define the height of the car.