Week 12- Final project
Development of a Door Trim panel - Final project
Aim: In this project we create the door trim panel Components that is (Lower substract,Arm rest, Bottle holder, map pocket) with the necessary input surfaces provided and generating the necessary B side features ( heat stakes, 4 way locators, Dog houses, push clips, Ribs, screw bosses etc) thereby assemble the individual components of the door trim by providing proper constraints there by performing the proper draft analysis using catia V5 software
Objective :
The main objective is to create the individual components of the door trim with input class A surface provided and generate the class B and class C surface and produce the solid surface body out of it and perform the proper draft analysis with required draft angle of 3 degrees for the body and continue the procedure for the remaining components .Then start creating the B side features of the components by following the reference of the master sections provided and perform the draft analysis with an input draft angle of .5 degrees and assemble the components to for the final door trim panel on the assembly workbench by providing necessary constraints using catia V 5 software
Procedure followed for the creation of the components:
- Analyse the input surface provided
- Class A surface as input surface
- Tooling axis creation
- Draft analysis of class A surface
- Class B surface creation
- Class C surface creation
- Solid surface body generation
- Draft analysis of the solid body
- creating the B side features
- Draft analysis of the solid body along with the B side features .
Class A surface:
Class A surface is an asthetic surface which is visible for the customer in the component
Class B surface:
Class B surface is an engineering surface where the B side features of the components like heat stakes, screw bosses, Ribs, doghouses are situated
Class C surface:
Class c surface lies as an intermediate surface between the class A and the class B surface thet means it generally accommodate the thickness of the whole plastic component
The input provided for the design is
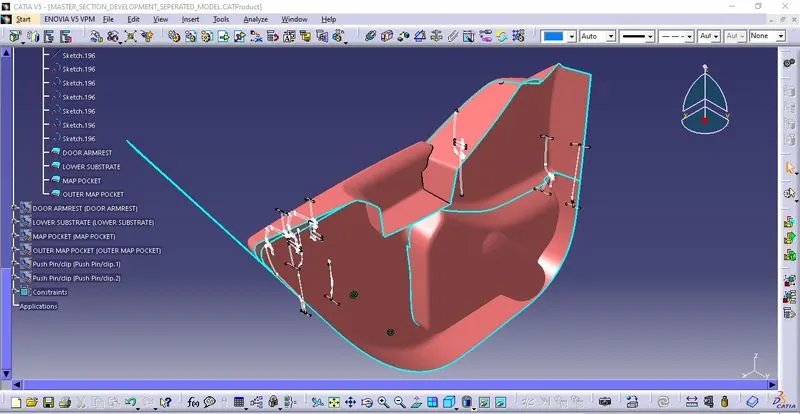
ARM REST DESIGN
In the front of the car, a central armrest, which commonly folds away based on user preference, will also often include a storage compartment and sometimes even cup holders. Some also provide the location for controls for non-essential functions of the vehicle, such as climate control or window motors.
For the Arm rest design the input class a surface provided is
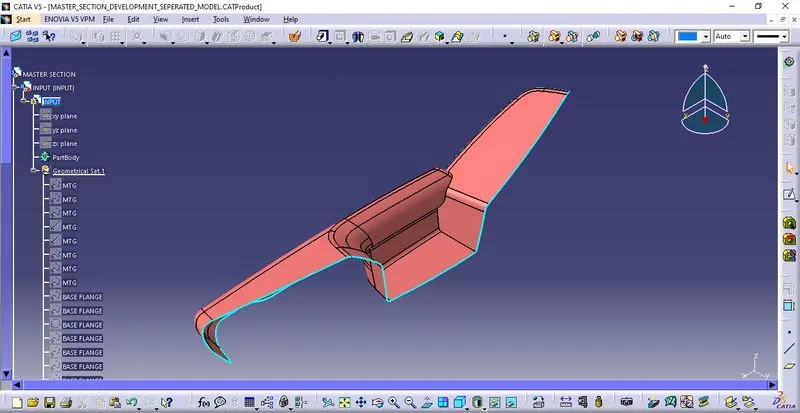
To check whether the surface has any open boundaries use the boundary feature then we can identify that there is an open patch or the surface which we need to work on
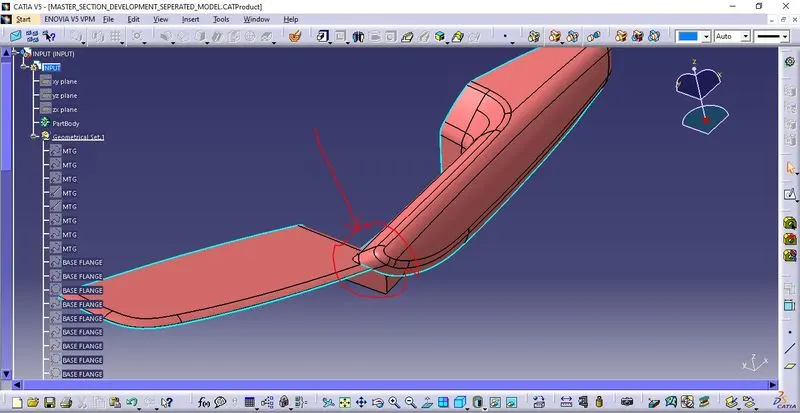
After solving the open patch
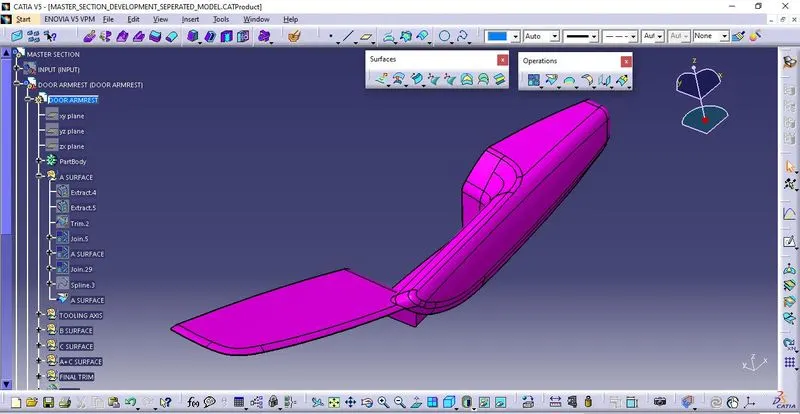
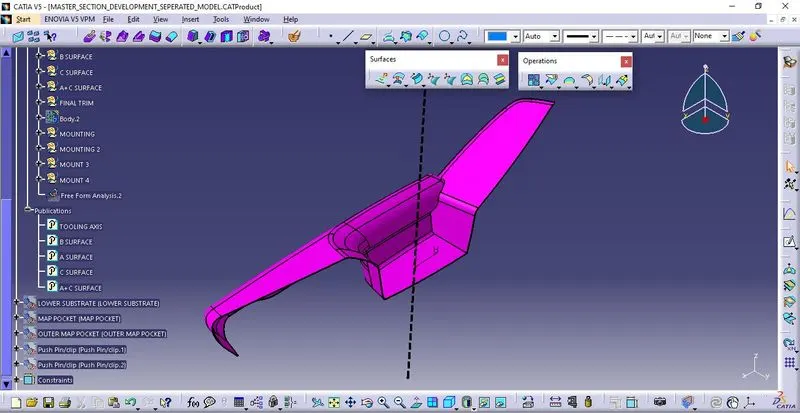
TOOLING AIXS CREATION :
In case of the arm rest we generally deploy the bisection methiod for creating the tooling axis , that is first we need to create a plane and form an intersection of the surface and generate the two lines from the intersection and there by creating a line by using the bisection method
Draft analysis of the class A surface:
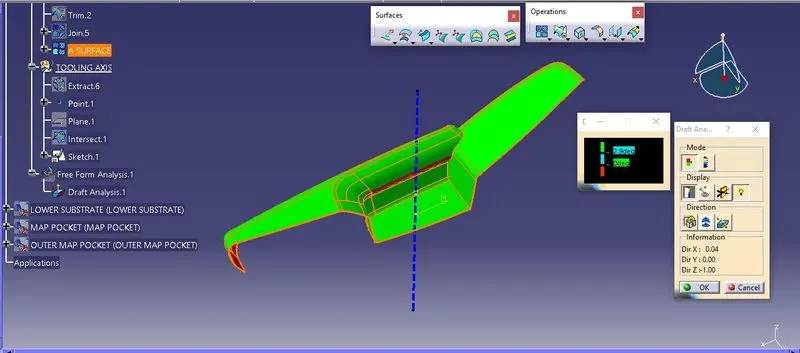
Once the creation of the tooling axis is done perform the draft analysis of the class A surf ae whether all the surfcaes of the clsss A is cleasring the draft analysis or not
General draft angle provided on the plastic engineerng componenet is 3 degrees
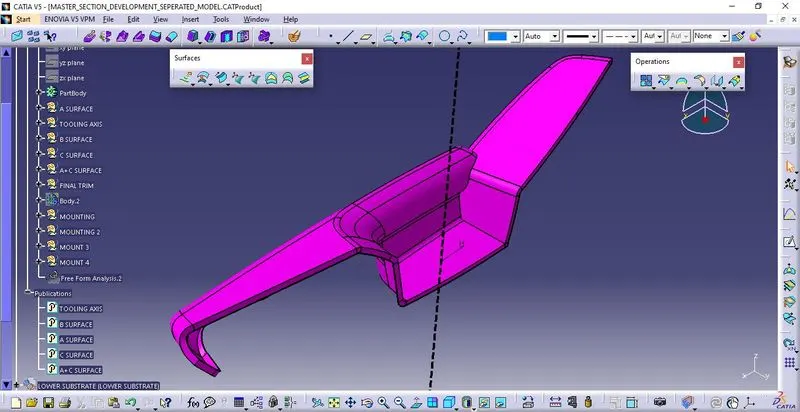
Generating of the class B surface
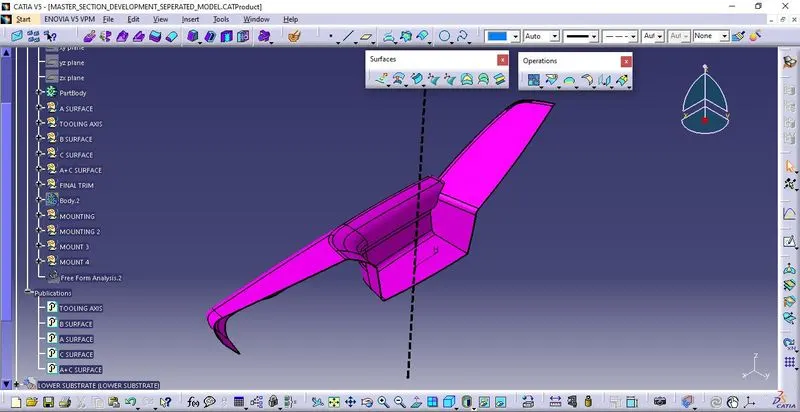
For the class B surface generation refer to the master section provided to measure the thickness of the plastic component then offset the class A surface to an extend of 2.5 mm thickness beneath the class A surface
Generating the class C surface:
For the class C surface generation we use the class A surface as an reference and follow the draft with respect to the reference surface and the main tooling axis
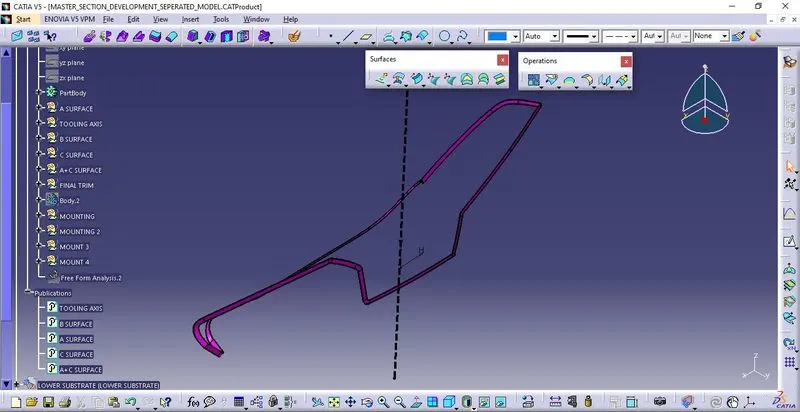
NOW join class A and class C with each other
Generating the final close surface:
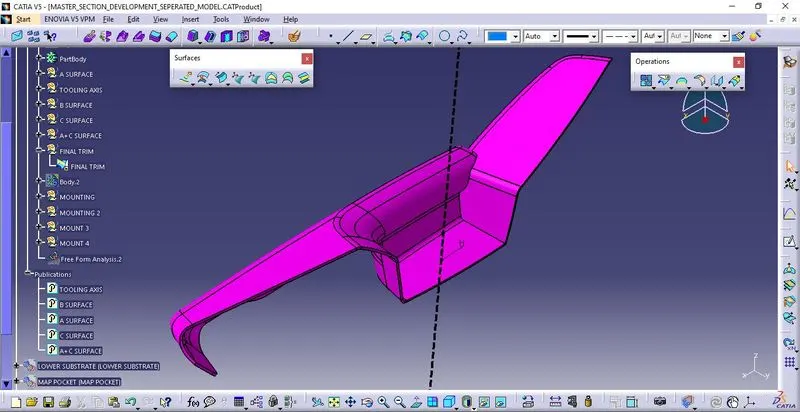
After creating the class B and the class C surfaces join the class A and the class C surfaces and trim the resultant with the class B surface then the resultant surface is the final closed surfaces
Creation of solid body
It is the close surface of the plastic componenet with a thickness of 2.5mm
Then create a new body and use the solid body feature to create the solid surface body out of it
Draft analysis of the final solid body :
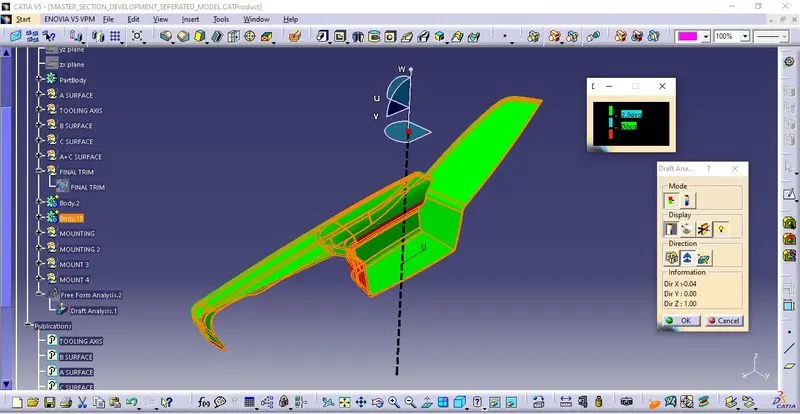
After generating the final closed body perform the draft analysis with a draft angle of 2.98 ~3 degrees
And examine whether all the required surfaces are clearing the draft with respect to the main tooling axis of any draft applied surfaces can’t be able to clear the draft analysis write a report mentioned what might be the reason for the surfaces not clear in the draft analysis and suggest the appropriate solution if else
LOWER SUBSTRACT :
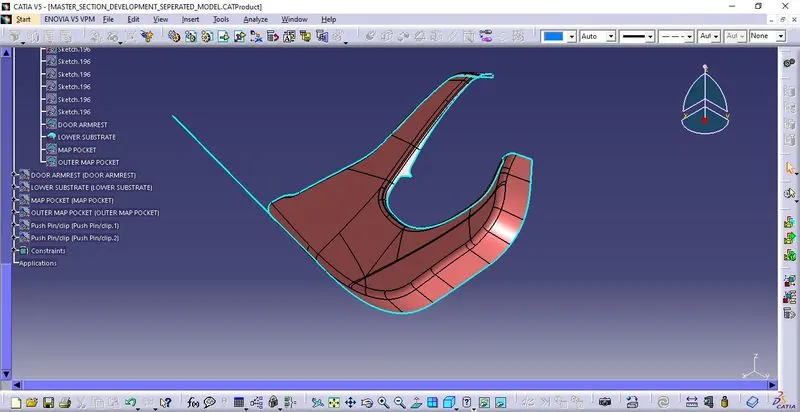
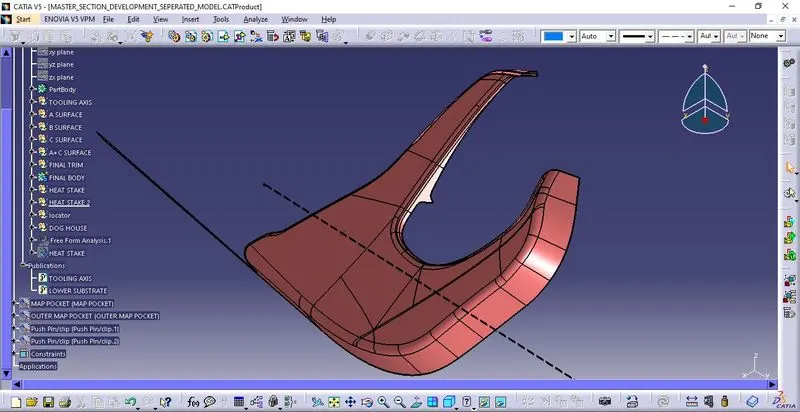
In case of the door lower substract after examining the provided input surface we can able to detect a projection or an extension so we don’t need it for any further so, create a line and split the unnecessary surface
Tooling axis creation:
Extract the surface from the class A where the surface is entirely visible and easy for the manufacturing by viewing the surface in different orientations
Now create a point at the middle At 0 coordinates and create a line in point and direction method and the create line is our main tooling axis
Draft analysis of the class A surface:
Perform the draft analysis on the class A surface to check whether all the surface are clearing the draft of 3 degrees with respect the tooling axis we create then continue with the model or if you notice any flaws notice them with the class A team to rectify or else continue with the class B surface creation
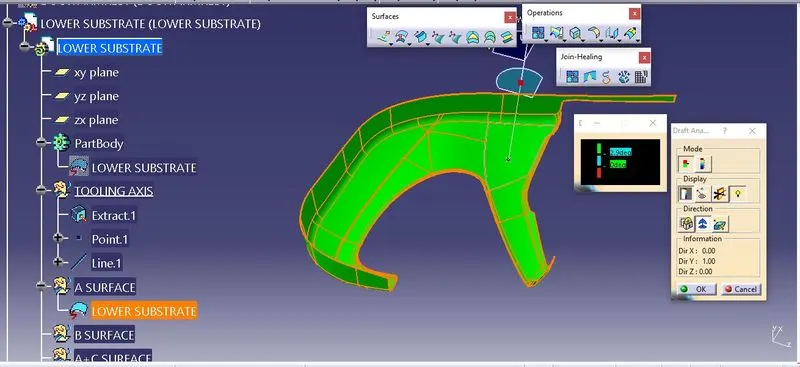
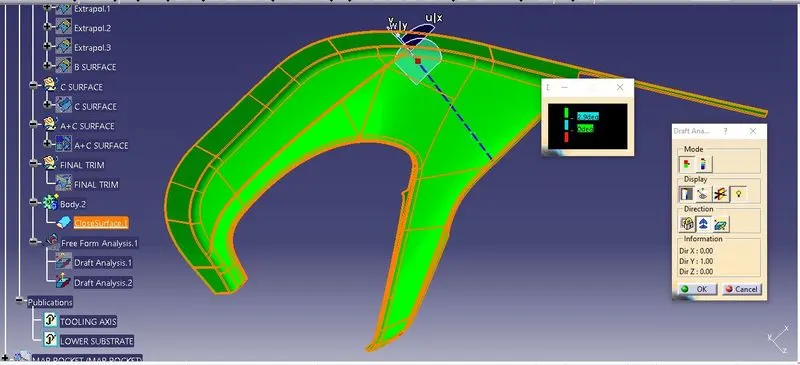
The class A surface is com[pletely clearing the draft analysis of the 3 degrees with respect to the tooling axis created
Creation of class B surface:
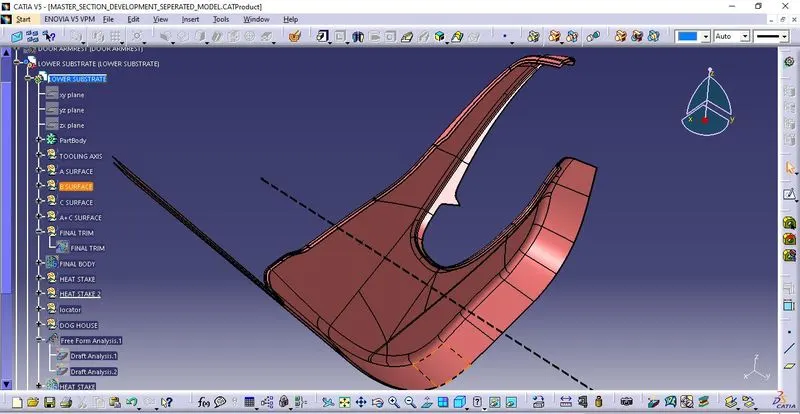
In case of the lower substract offset the class A surface to a value of 2.5 mm beneath the class A surface then extrapolate the class B surface which would help to make the final trim with the class A and C combined surface
Creation of class C surface :
When the surface of the class C is parallel to the tooling axis then make use of the sweep with respect to the draft Direction to an angle of 3 degrees and the surface need to be outside the class A surface when seen from the normal direction with respect to the main tooling axis. And if the class C surface which need to create is perpendicular to the tooling axis then make the sweep with the reference surface With 90 degrees or with 87 degrees
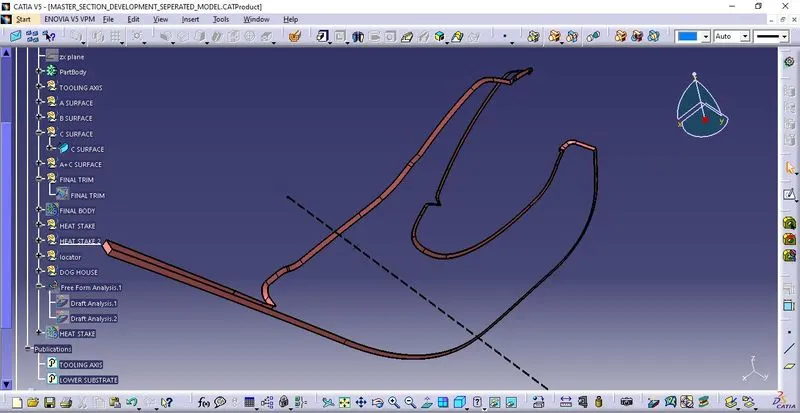
Final surface formation:
Now join the class A surface with the class C surface and trim the class B surface with the join A and C surface
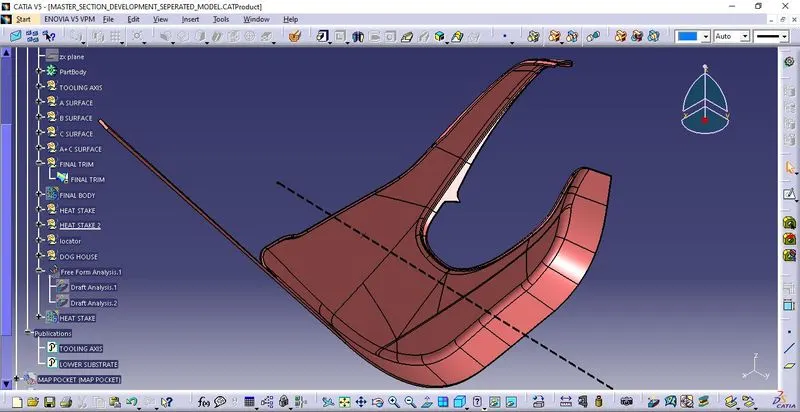
Solid surface body formation:
Now go to the part work bench and use the solid surface feature to create the solid surface body
Draft analysis of the solid body:
Preform the draft analysis on the solid body with a draft angle of 3 degrees and see the results
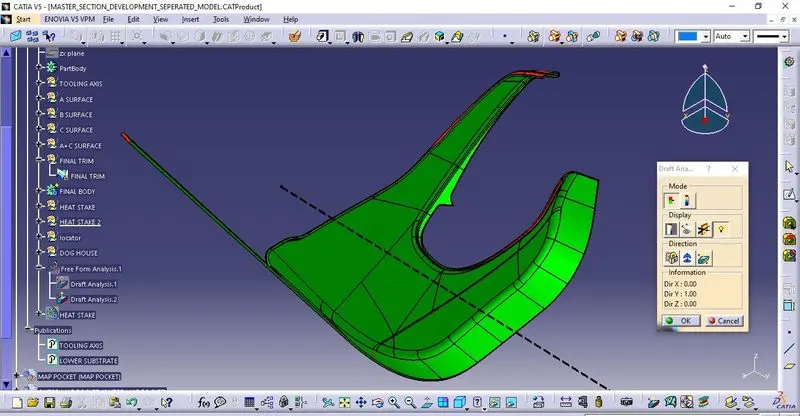
Some of the surfaces are generating the negative draft or the draft angle less then the 3 degrees
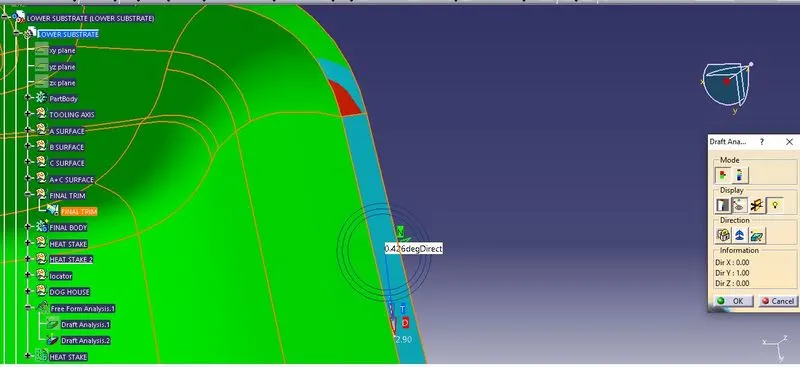
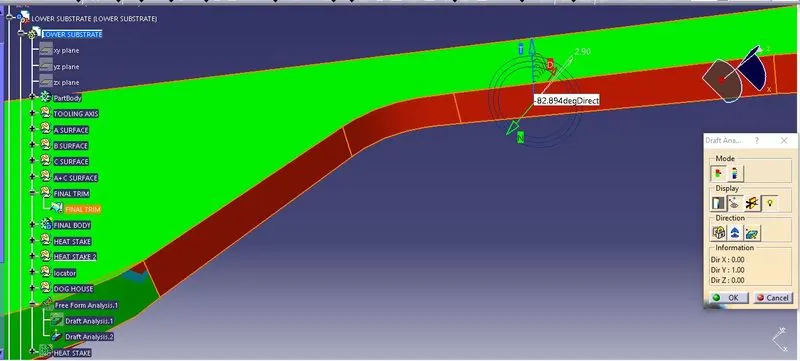
These type of deviation in the draft angle on the surface is mainly due to the quality of the class A surface provided , if we manage to provide the correct draft it will lead to the distortion of the class c surface which leads to the difficulty in manufacturing the component so, report the above draft analysis of the solid body to adopt or alter the proper changes in the class A surface team
MAP POCKET DESIGN :
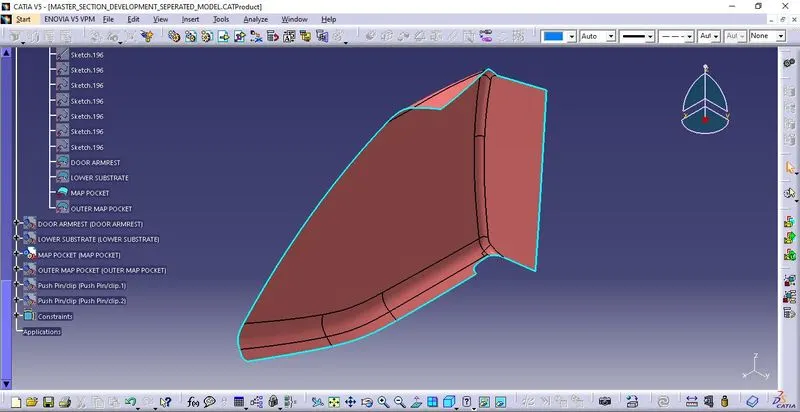
Map pocket is the sub element situated right at the hub of the lower substract of the door trim panel . The processs illustrated is same as the prevous components first, we need to check the boundary of the given input surface whether there might have any open patches or else protrude the input surface as the required class A surface
Tooling axis creation:
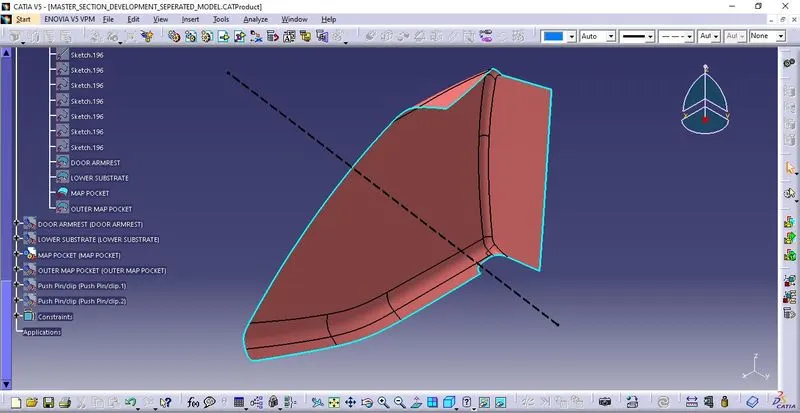
In case of the map pocket the we extract the surface in the Y direction orientation and use the point - direction to generte the tooling axis of the map pocket
Draft analysis of the class A surface:
Once the tooling axis is create analyze the draft for the class A surface with a draft angle of 3 degrees
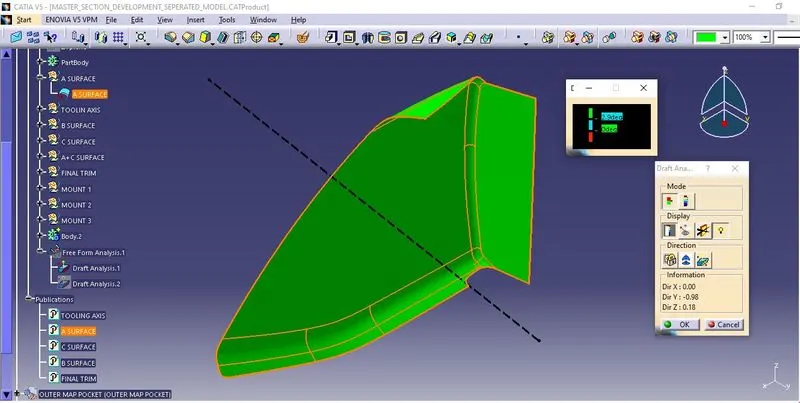
So, its perfectly clearing the draft of 3 degrees with the generated tooling axis
Class B surface creation:.
Now step forward to create the class B surface deploy the 2.5mm offset of the class A surface to generate the class B surface beneath the class A surface
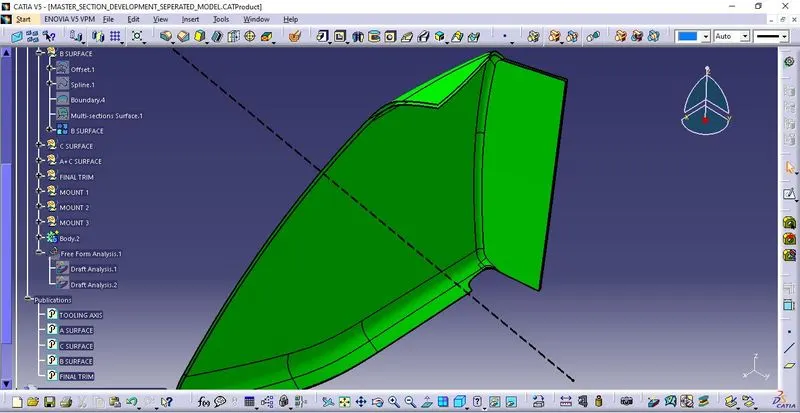
Class C surface creation:
Now create the class C surfcae which is an intermediate surface between the class A and the class B surface generally like a fill between the two surfaces created with the help of the sweep feature with a draft of 3 degrees
along the tooling axis direction and with a draft of 90 degrees along the reference surfcae sweep
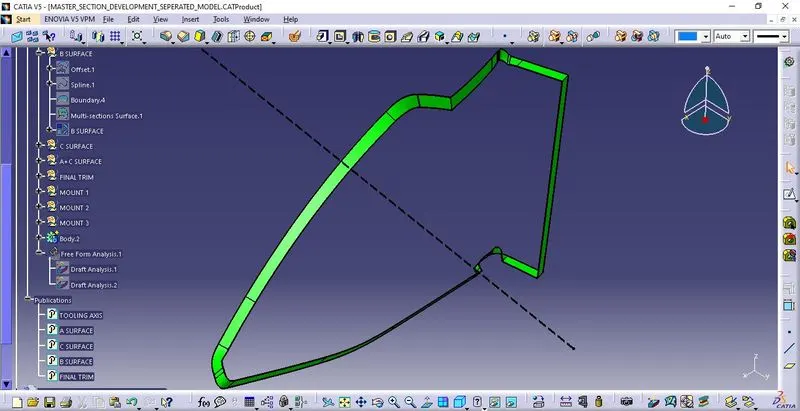
Final surface creation:
Once all the surfaces are created that is the class B and the class C surfacesthen join the class A & class C surfcaes and trim the join surface with the class B surfaceto form the final closed surface
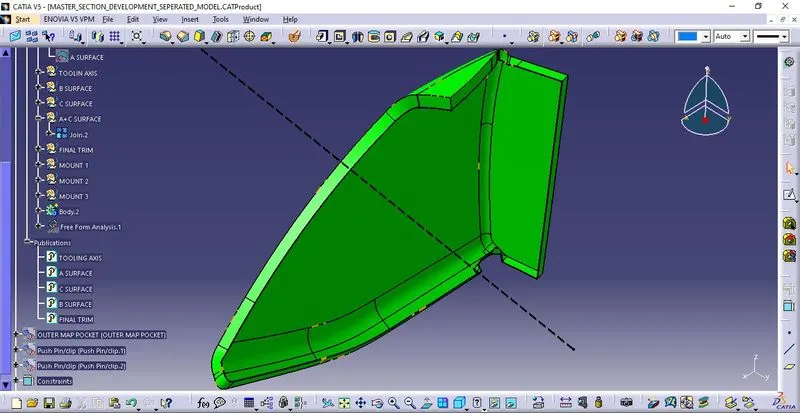
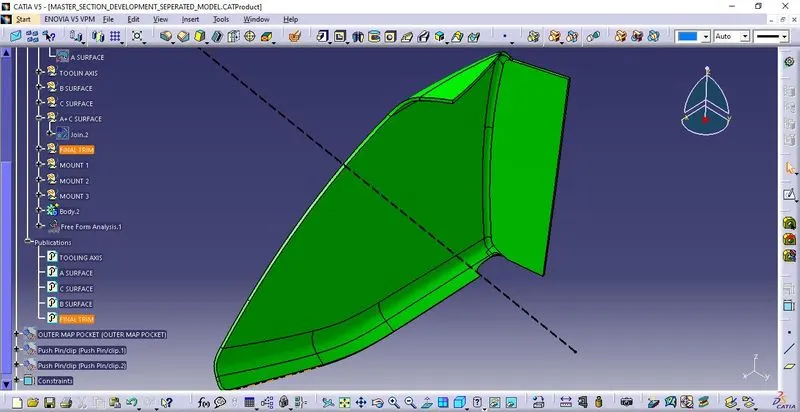
Draft analysis of the solid body:
Now perform the draft analysis with a draft angle of 3 degrees on the solid body
The results obtained are
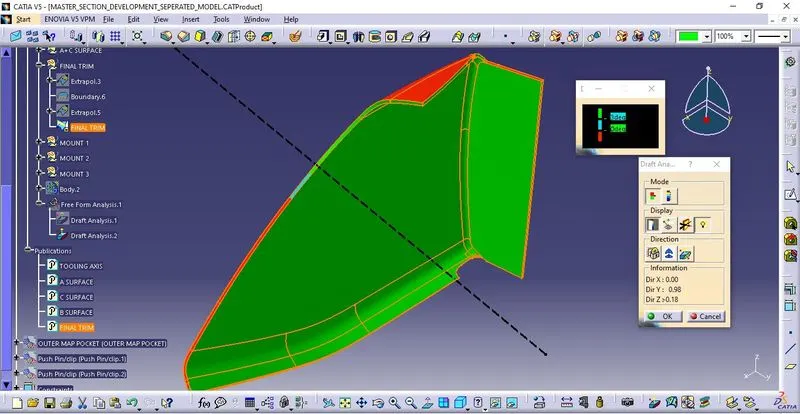
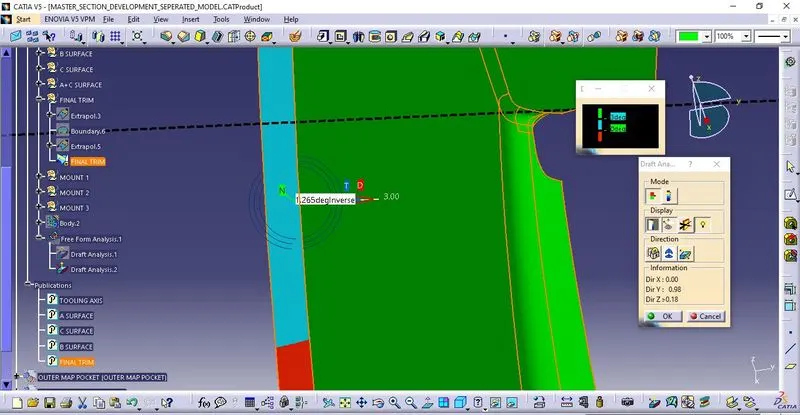
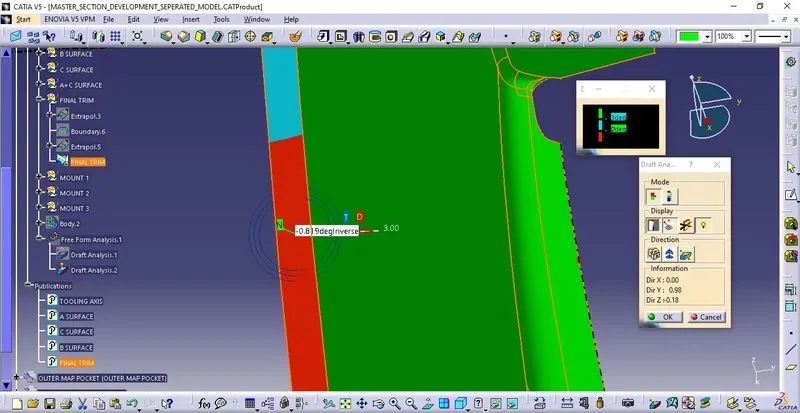
Almost all the surfcaes are clearing the draft of 3 degrees along ther B side but some of the surfaces thet leads to a lower draft opr the negative draft mainly these issues rise when there is an issue with the class A surfcae .Here the class a draft is perfect but the curvature of the class A surface at the corner edges is not that much good, so during the class C surface generation the class c might not be that perfect to claer the draft angle of 3 degrees if possib;le to manage the surface to clear the draft the quality of the curvature formed at the corner or at the irregular curvature is impossible to manufacture So, make areport regarding issuesx due to the curvature defects and repoort the draft defects to the class A team so they will make the necessary adjustments in the class A surface if necessary
BOTTLE HOLDER DESIGN :
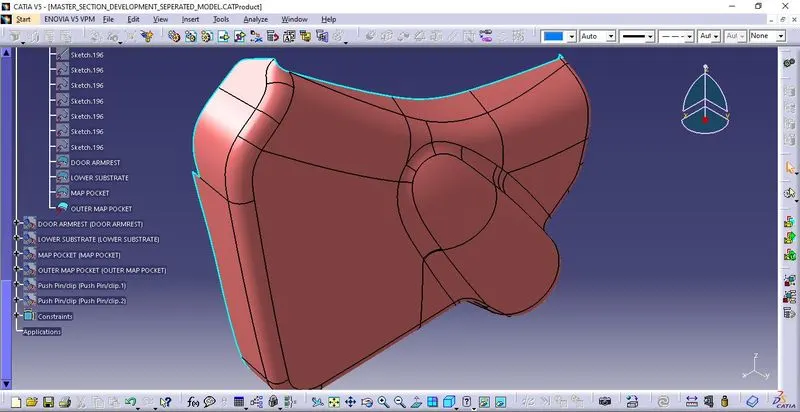
The input surface provide for the bottle holder is
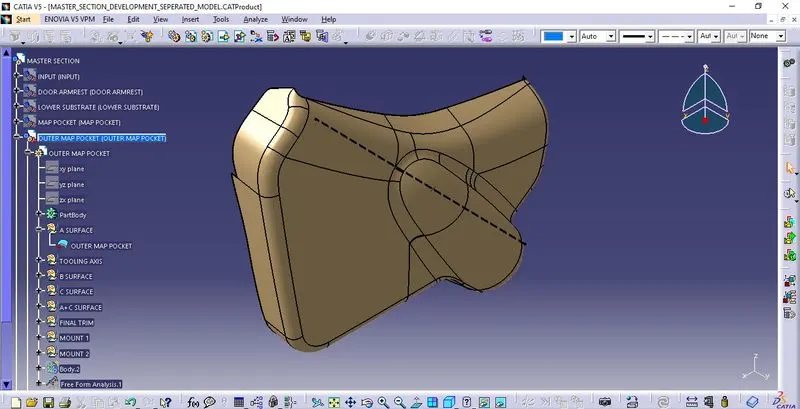
Tooling axis creation:
In the case of the bottle holder use the flat surface and extract the surface and create a point at the 0 coordinates and use the point - direction to create the tooling axis
Draft analysis of the class A surface :
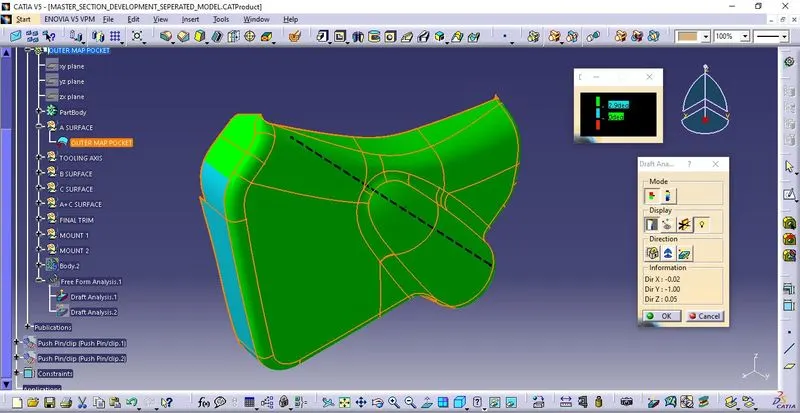
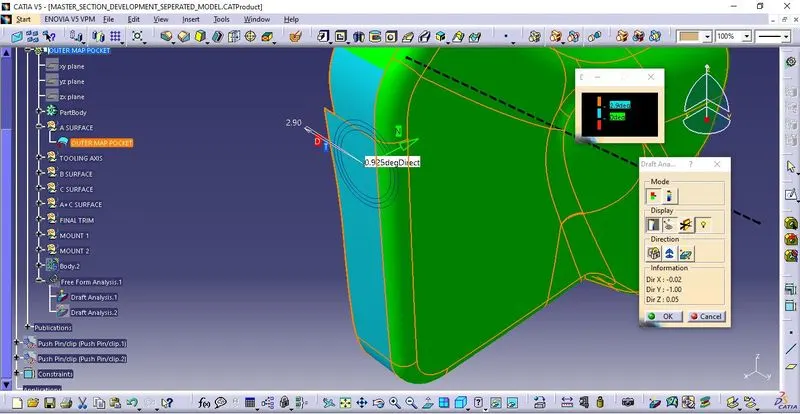
Perform the draft analysis of the class A surface with a draft angle of 3 degrees the result obtained is
Class B surface creation:
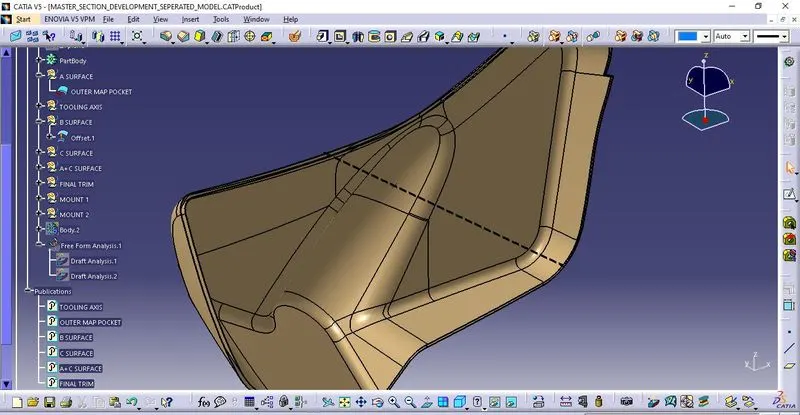
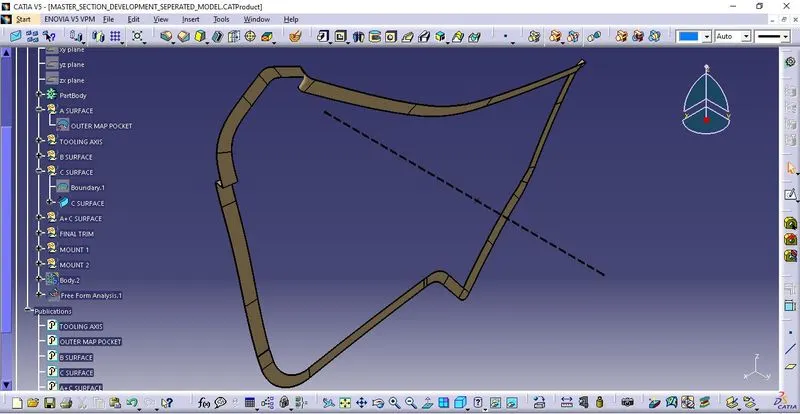
Now offset the class B surface to 2.5mm following the master section beneath the class a surface and extrapolate the class b edges to an extent to form the proper ytrim with the class A and C join Choose the correct direction for offsetting the surface
Class c surface creation:
Now create the class C surface with the aid of the class a surface and the sweep feature along the draft direction and the reference surface parameters . So provide adraft of 3 degrees along the draft direction making the direction of the draft as the main tooling axis and 90 degrees draft with rreespect to the reference surface
Final surface creation :
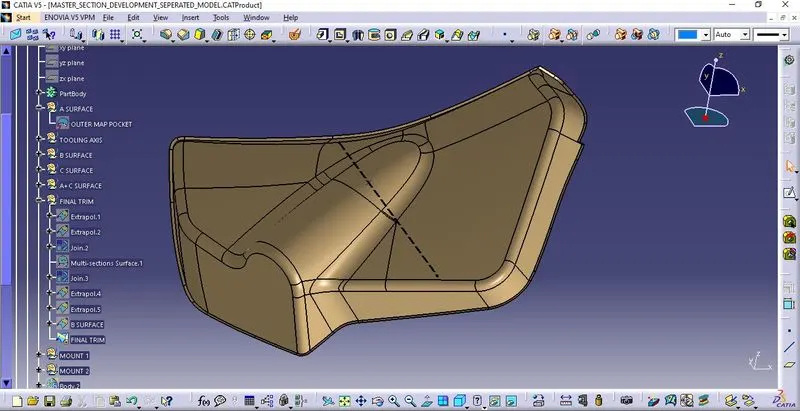
Once all the surfaces are created that is the class B and the class c surfaces join the class C surface with the classs A surface and trim the joined surface with the class b surface
Solid surface creation:
Once the closed surfae is created then go to the part workbench and use the solid surface feature to generate the solid body out of it
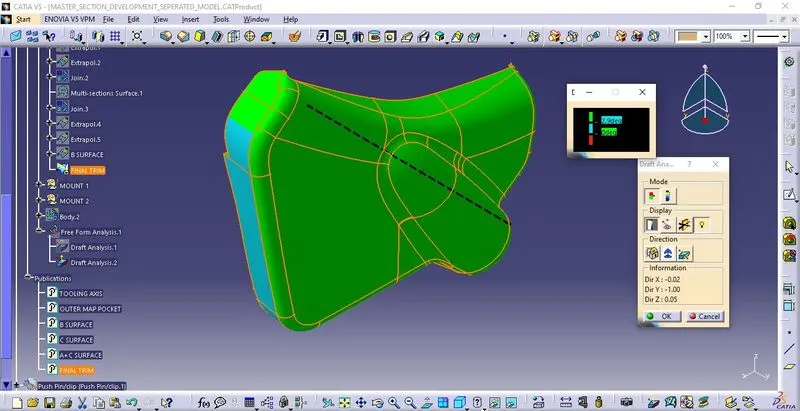
This negative draft is mainly due to the inclined curvature edges and the improper continution of the edges along the surfaces these are the changes that need to be updated and rectified by the class A surface input team
B side attachment features:
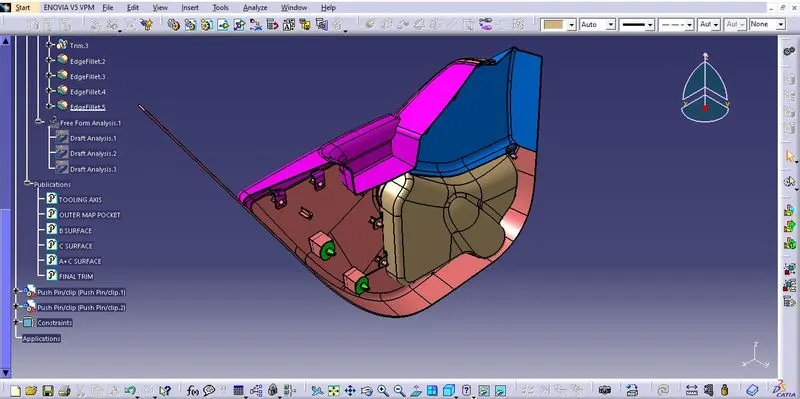
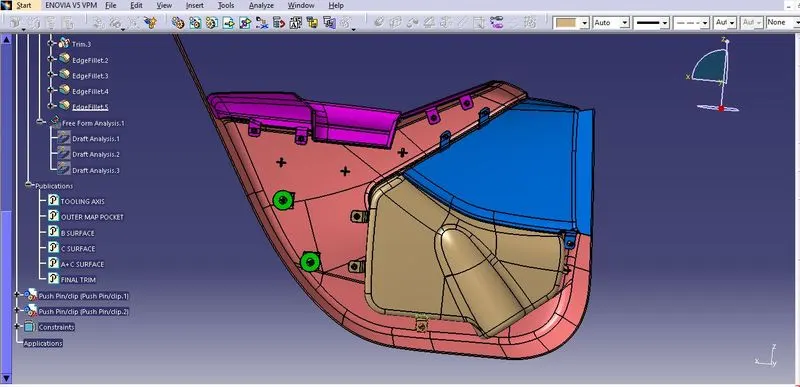
Once all the solid bodies are completed the assembly would be like
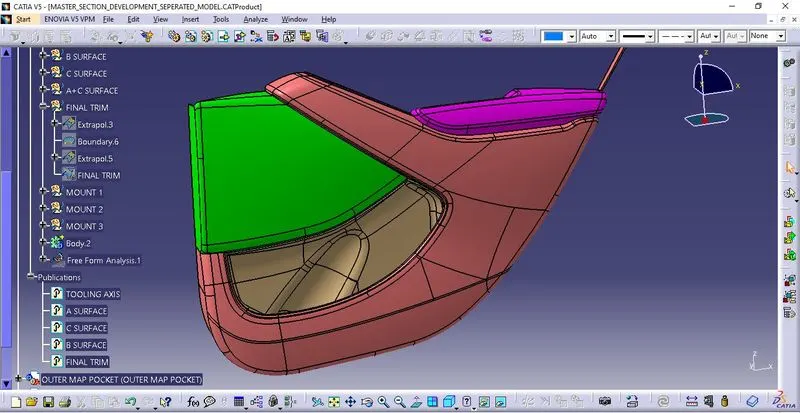
The input surfaces of the door trim panel provided is
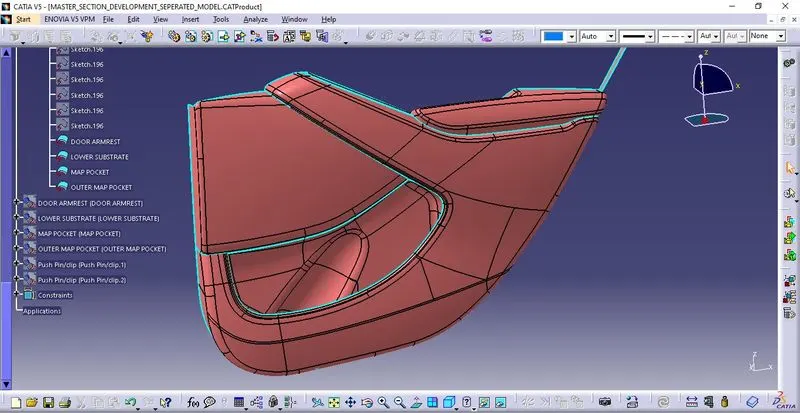
so for the final solid surface components we need to provide thye proper attachment features by adopting the industry design standards sand design parameters considerations
AS a design engineer we need to have an idea regarding how a component need to connect wityh the adjacent component either by the flanges and the heat stakes assembly or with the flange and the locator assembly or with the dog house and the push pin etc
So we need to move step by step for creating the proper attachment features on each and every individual components of the door trim panel for the assembly of the component
Lower substract attachment features:
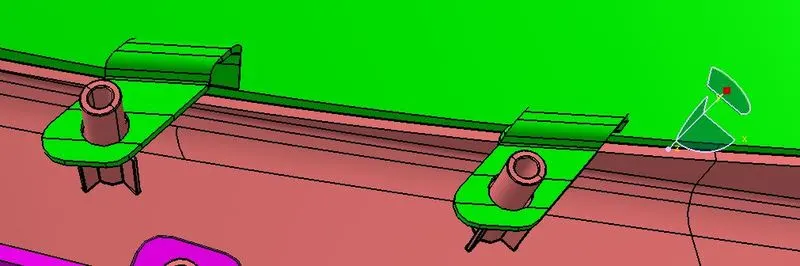
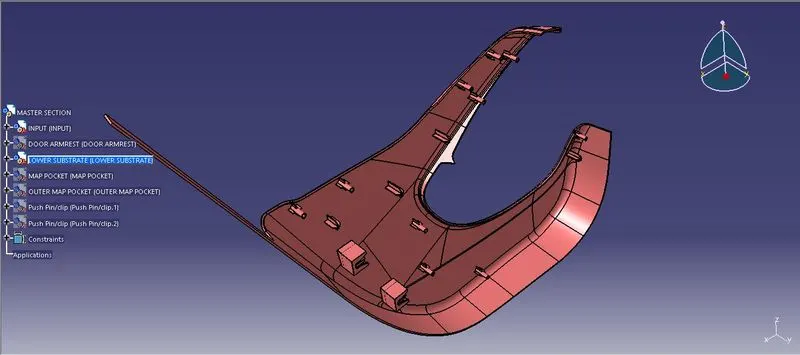
Based on the master sections provided for the for the input surface of the lower substrate it indicates theat the heat stakes are positioed on the surface
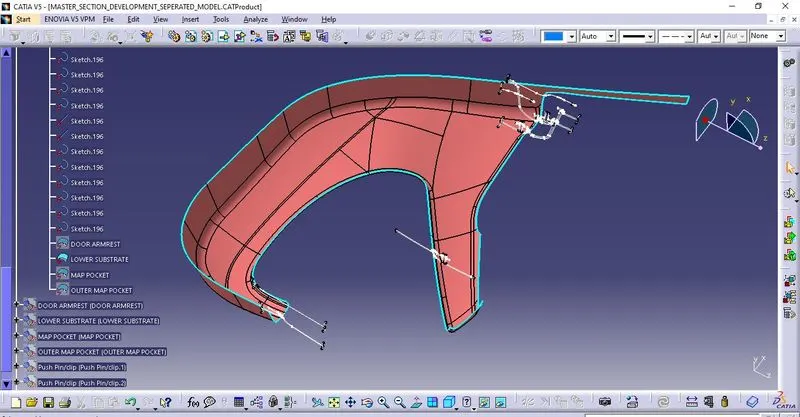
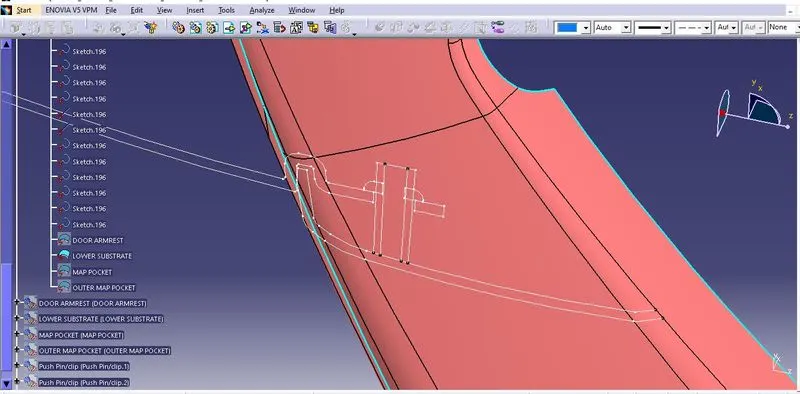
Following the master section wee need to create the heat stakes on the lower substract B side
Heat stakes :
Process for heat stakes assembly:
In thermal staking, also referred to as “heading or riveting”, the controlled flow of the molten plastic is used to capture or retain another component, usually of a different material.Thermal staking provides an alternative to welding when the two parts consist of dissimilar materials which cannot be welded or when simple mechanical retention of one part relative to another is adequate .
The most commonly used application involves the attachment of metal to plastic. A hole in the metal part receives a pre-molded plastic boss. The thermal tip contacts the boss and creates localized heat. As the boss melts, the light pressure from the horn forms a head to a shape determined by the horn tip configuration. When the heat is terminated, the plastic material solidifies and the dissimilar materials are fastened together.
So taking the references from the master section here we need to make a note of that whenever we take the reference from the master section the referenced elrement should be isolated from the master section
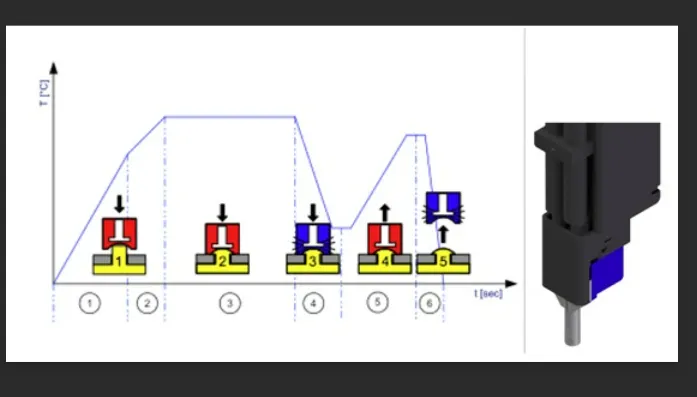
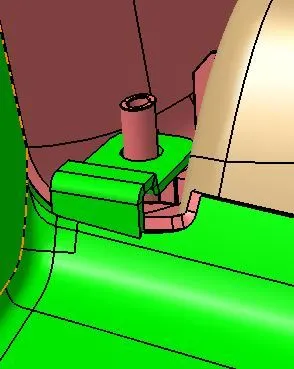
so start working on the heat stakes creation and provide the support it with ribs on the four sides to add additional strength to the heat stake
CREATING THE ATTACHMENT FEATURES FOLLOWING THE MASTER SECTION.
Design parameters:
- Height we need to follow the master section
- Draft provided on the outer and the inner face with an angle of 0.5 degrees
HEAT STAKES
- Heat Staking is a pulsed-heat process to join two or more parts out of which one at least is made of plastic.
- The process is to deform the plastic material using heat and force at a set process time.
- The bond is made by partially de-forming the plastic part in order to fix the other.
- Heat Staking makes it easy to bond metal to plastic and is commonly used in high volume/low cost applications such as automotive, IT and consumer appliances.
- Similar and dissimilar materials may be joined: metal to metal, plastic to plastic, metal to plastic
- Accurate control operating within a small process window
- Local heating resulting in no damage to surrounding materials
- Processing of glass-filled materials
- No mechanical vibration
- Many heat-stake shapes possible through custom designed tools.
RIBS
- The ribs provide economical stiffness and strength to the part without increasing the overall thickness of the part.
- The ribs are used as locating and arresting in the assembly as locators.
- Proper allignment in mating parts, slot and rib pair is long lasting other than screw pair which loosen up with time.
- Acting as stops or guide for mating the tilted headlamps.
- Rib designs includes.
- thickness, quantity, height , manufacturibility and location.
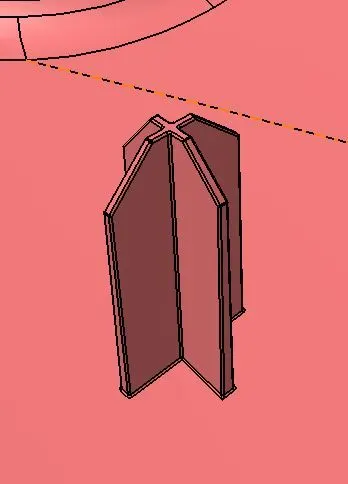
Locators:
- Locators are used to locating the position of the mating part while assembling.
- The design rule for the locator is mostly the same as the rib but the height of the locator should be more than the heat stakes at a min of 5mm.
- The locator also constrains the movement of the mating part.
- The gap between Flange and the locator should range between 0.5mm and 1 mm.
- There are two types of locators.
1. 2-Way Locator.
2. 4-Way Locator.
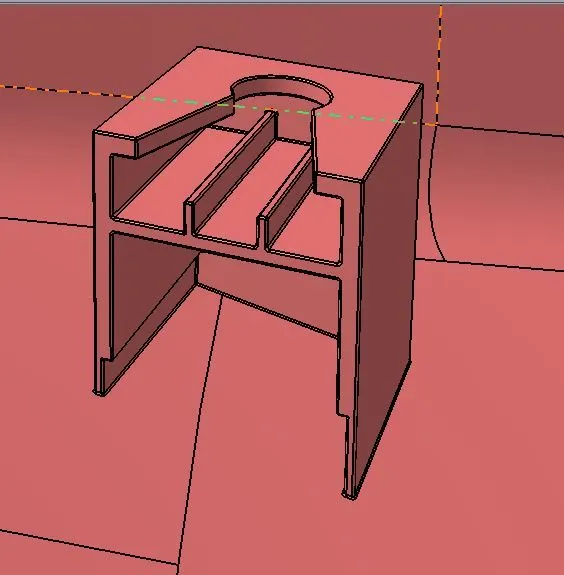
DOG HOUSE
- Dog house is the attachment feature which helps you to assemble things at certain heights and also resolve the plastic defects.
- There are plenty dog house design which can be used for assembly purpose but we will be using the one provided to ous by the resources.
- The master section or the enginnering drawing must be followed for creating the dog house.
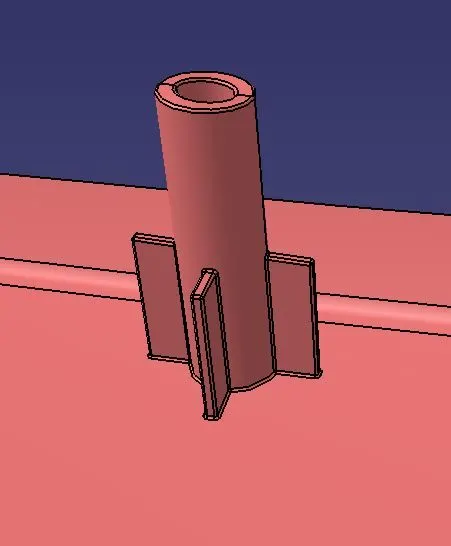
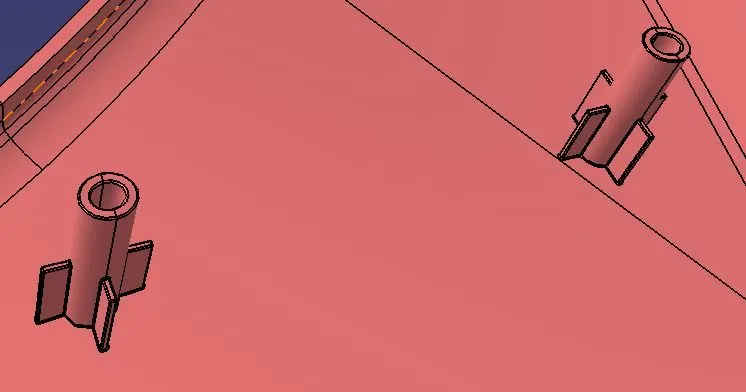
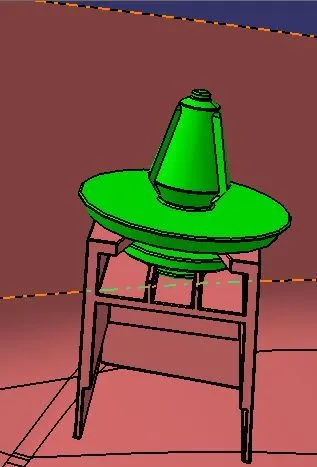
PUSH PINS
- These pins are used for the assembly purpose .
- These pins are guided into the sheet metal body.
- The pin is assembled over the dog house on one side and other into sheet metal
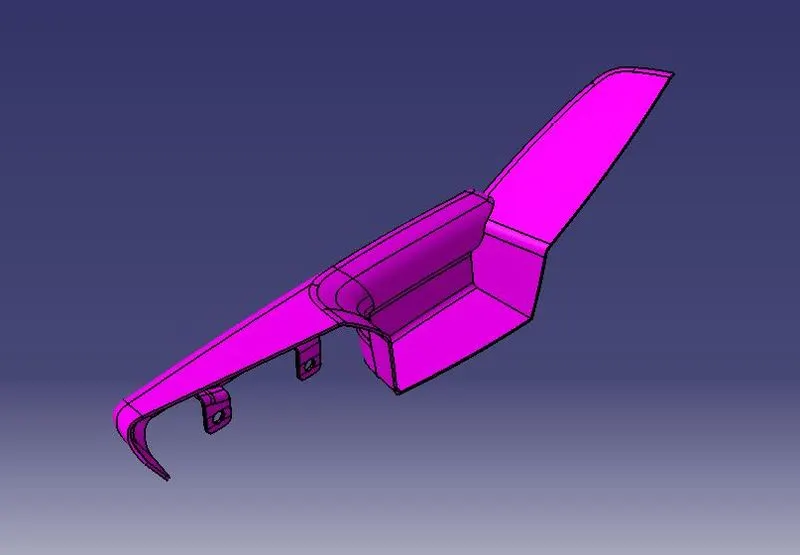
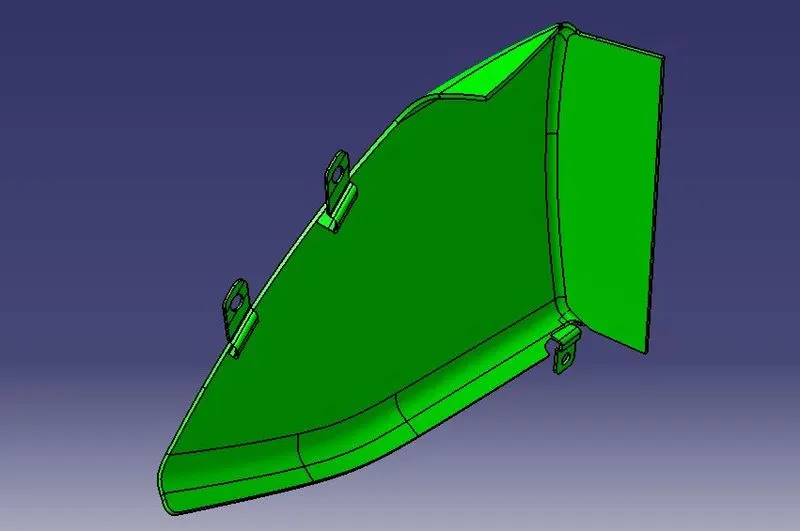
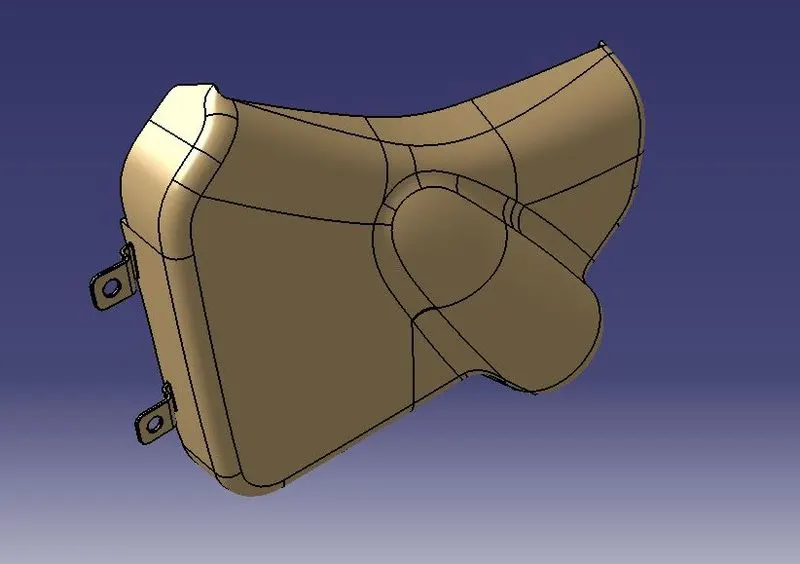
FLANGES ON THE COMPONENT
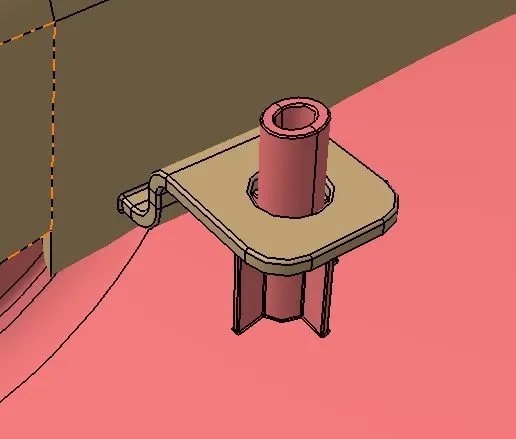
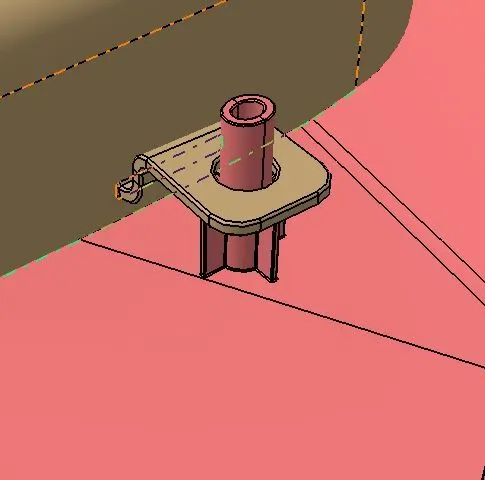
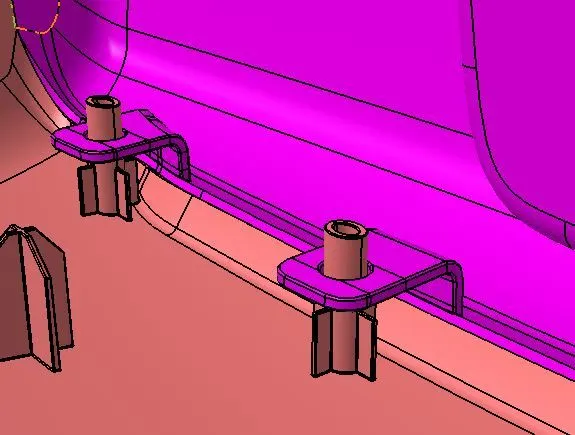
- These flanges will be build on the components for the fittment purpose with lower substrate.
- The hole at center will be guided along the heat stakes.
- Later top portion of the heat stake will be melted over it.
- The flange should rest on the supporting ribs on side .
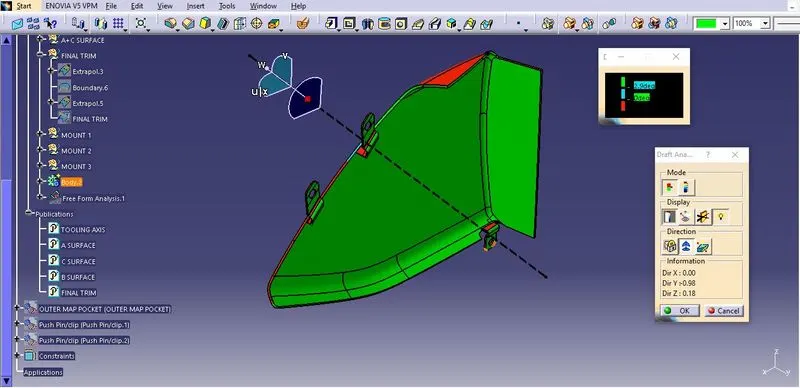
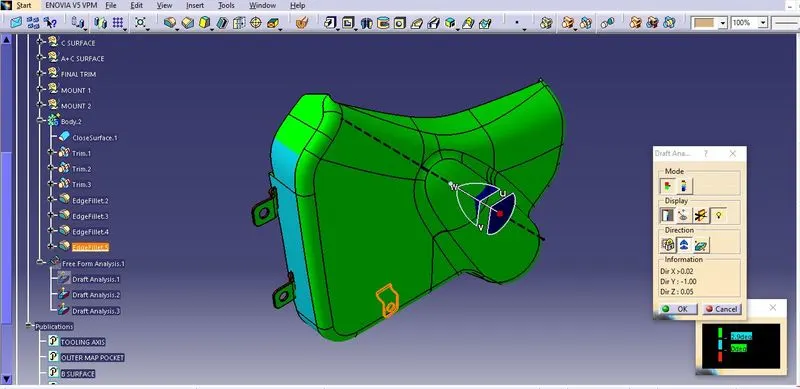
DRAFT ANALYSIS OF THE COMPONENTS:
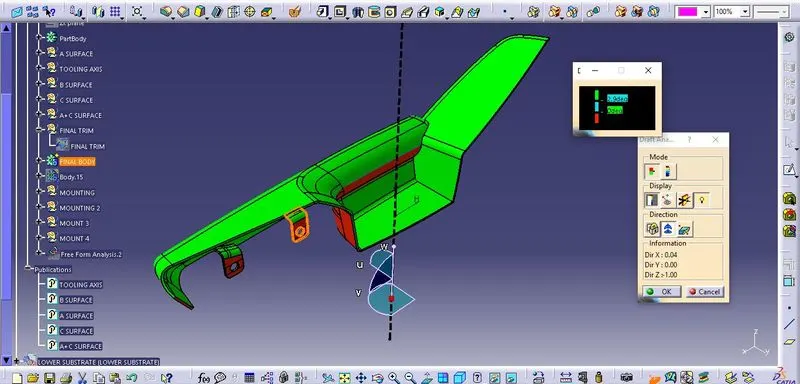
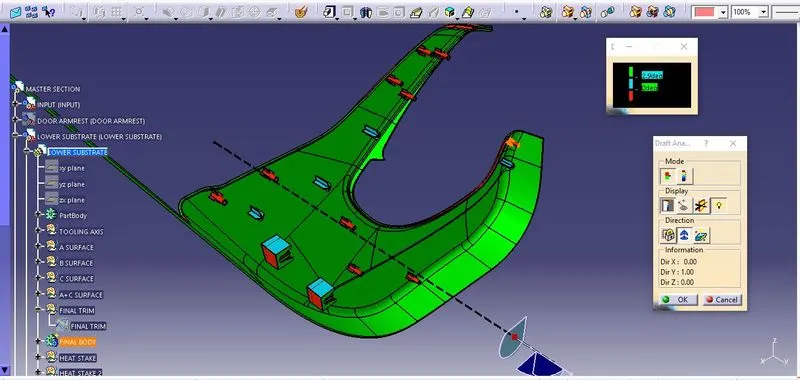
- The draft analysis is done to ensure that the draft in permeasible with the design consideration.
- The draft analysis is done by changing the visualization mode to customize and select shading as material.
- The draft based feature enables us to visualize and examine the draft.
- The draft window is has two tables one is for examining the draft and other one is the colour code.
- The draft value is set in the colour code window with each colour having their own significance.
- The red colour indicates the positive draft less than minimum draft where as the green colour indicates the minimum draft.
- The blue colour indicates the negative draft.
- For visualizing the draft the compass is aligned with the tool axis direction and the cursor is then made clicked upon the surface for viewing the draft.
- The quick view in display window enables to examine the draft value throughout the surface.
- Here both class A and closed body are given the minimum draft as 3 degrees.
- The attachment feature are given draft of 0.5 degrees.
FINAL OUTPUT :
CONCLUSION :
The Design of The Automotive Door Trim Panel from a Class A surface to a Closed Part Body with all the necessary attachment features by following all the design rules using CATIA V5 is done Successfully and all the required CATPart and CATProduct files are attached.