Week 10 - Challenge 3 - Door Trim Lower with Engineering Features
Objective:
Create the Door Trim Lower Plastic component through the given Class-A surface. To begin with, the tooling axis for the given Class-A Surface should be created meeting the requirements of the draft angle and at the end perform the Draft analysis on the model.
Create the Heat Stakes and the locators considering the design rules mentioned in the video for the door applique.
PROCEDURE:
1. Open the given class A surface. Ensure that all its boundaries are connected.
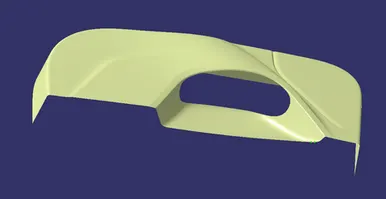
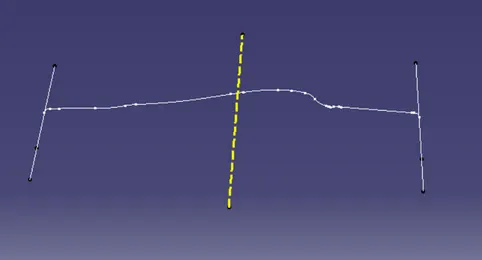
2. Tooling axis: To create the tooling axis, extract a surface from class A and create a point in the middle of the surface by using the point command and create a line at that point through the axis which looks a better path for the tooling direction. Now, name this line as the dummy axis. Create an axis system on the point created. Intersect the surface A and the planes from axis system. Now, create the lines at the ourter most side the surface which are int he direction towards the dummy tooling axis creater earlier. Bisect the line to get the tooling axis.
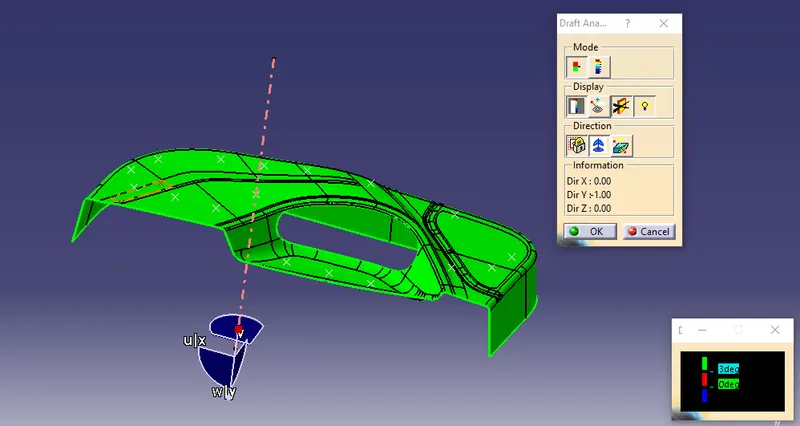
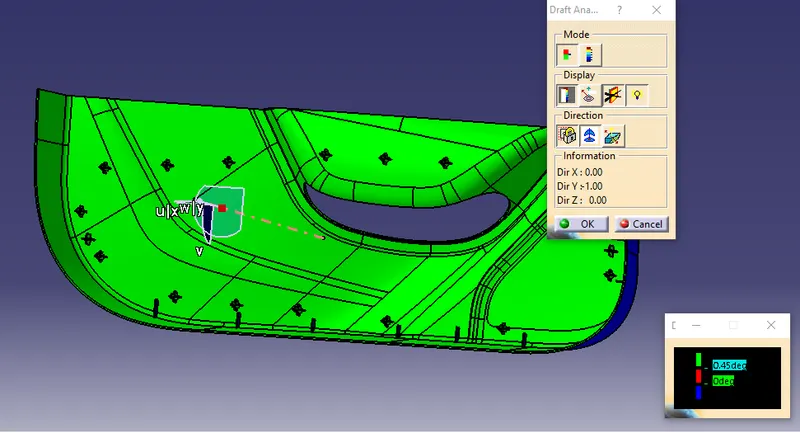
3. performed a draft analysis check from that line whether the created tooling axis is in the correct position or not. If in the draft, analysis check the surface highlighted with green colour on both sides of the surface the tooling axis is in the correct position and direction.
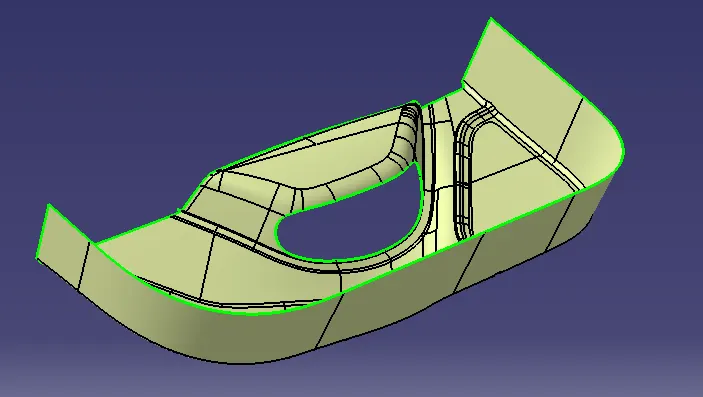
4. Create a B surface at an offset of 2.5mm with respect to the A surface given. We can notice that few of the elements will be missing after offset. Using features like the extract, extrapolate, multisection etc, fill up the missing elements.
The B surface will look as below after following the above procedure.
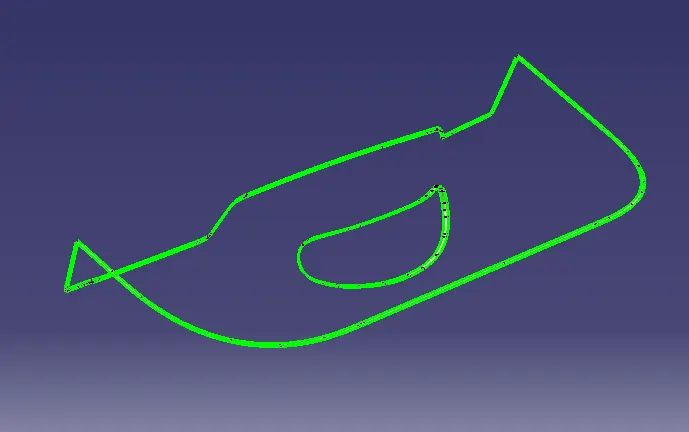
5. Using Sweep option Create the C surface as shown below.
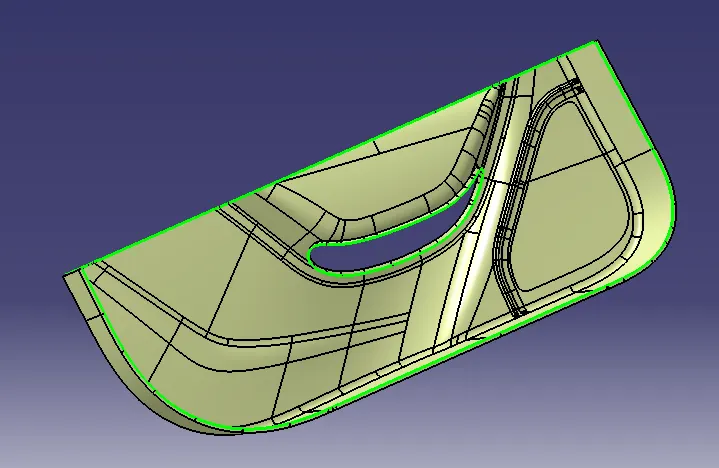
6. Join the C surface with the A surface.
7. Trim the B surface with the above surface to obtain a closed hollow body using surfaces.
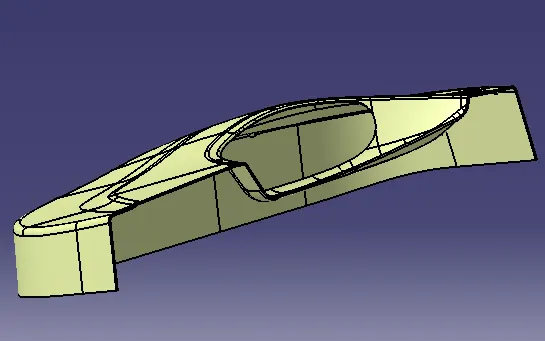
8. Convert the surface body into part body using the feature close surface.
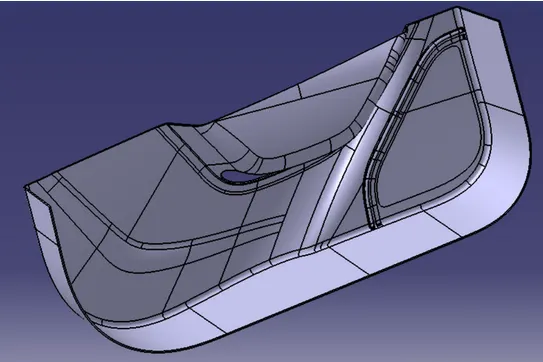
9.Draft Analysis:
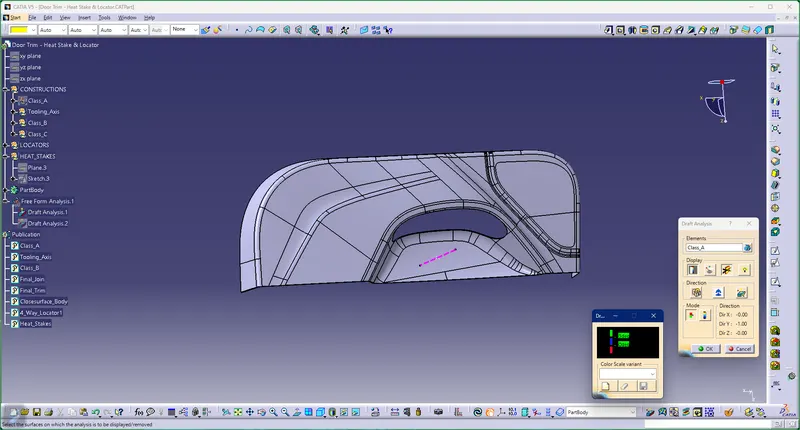
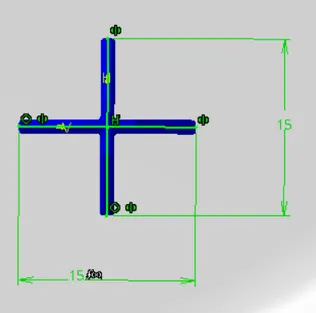
10. Create a 4 way locator using a sketch on the body. After creating the sketch, pad it 20mm in height and thicken it to 1.3mm and draft it with 0.5deg in the direction of the tooling axis. Give 5mm of chamfer with 45deg of inclination and a fillet of 0.20mm radius.
Use copy and paste the 2 nd 4 way locator using the translate feature.
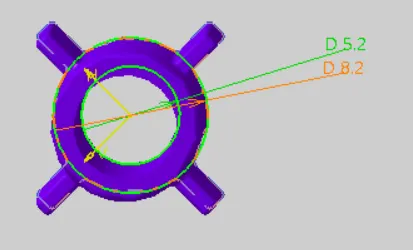
11. Create Heat stake. Draw a sketch on the surface. After the creation of the sketch, Pad it to 18mm height and a draft angle of 0.5deg on both sides (inside and outside) and then provide a fillet with a 0.20mm radius. After creating the heat stake, create the ribs for supporting purposes. To create the ribs, draw a sketch and padded it to height less than that of the heat stake and 1mm in thickness. After padding the ribs, drafted 0.5deg in the tooling axis direction and fillet it with a 0.20mm radius. Finally, use union trim on the ribs with a heat stake to remove the ribs as per the requirement, which are present inside the heat stakes.
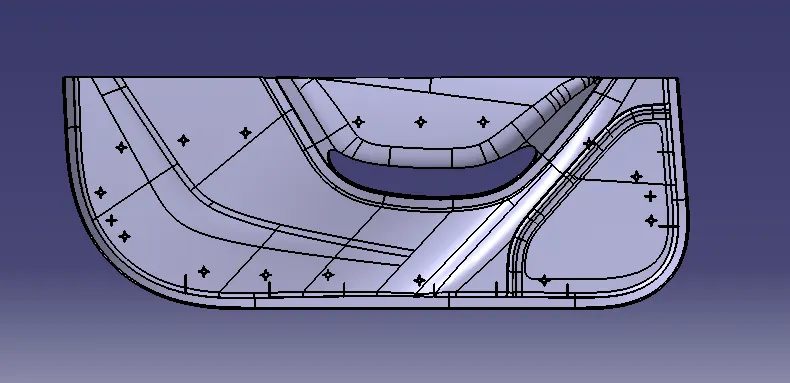
Copy and translate the heat stake to all the positions as needed.
12. Create ribs as shown below.
13. Perform draft analysis on the part. for inspecting the features which are added later on the B surface.
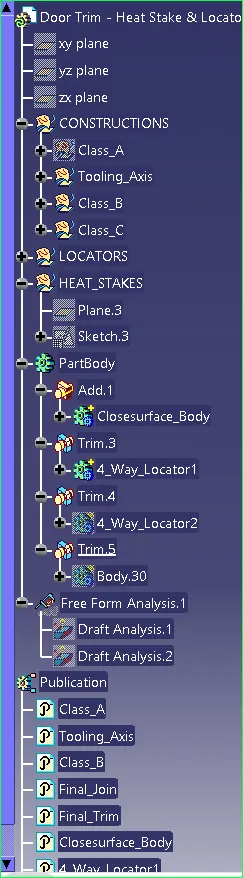
TREE STRUCTURE:
From above we can find that the componen is manufacturable.
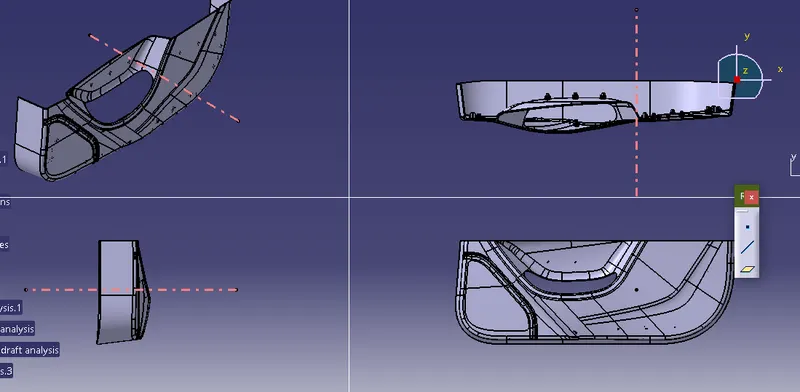
Views:(isometric view,front view,left view,rightview,top view)
From above we can find that the componen is manufacturable.
CONCLUSION:
Thus by following the above we crate the door trim with B class features (heat stake and locator pins).