Week 1:- Introduction to BiW and Fixtures Challenge
1. BIW
Body in White, or BIW, is a stage in the production of automobiles in which all sheet metal components such as the roof, body side, under body, backdoor, cross members, and other components are welded together and the resulting body is dipped in a primer solution, which has a greyish colour and thus gives the body its name. The car's shape is determined by the BIW, which is obtained after welding and before painting.
BIW consists of;
- Body side
- Under body
- Closures
- Roof
- Fender
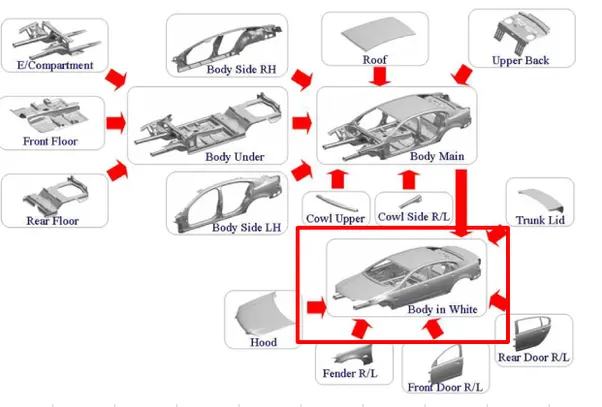
Body Side Panels
- A-pillar- A-Pillar is the front most support to Roof.
- B-pillar- B-Pillar is the second support to the roof and situated on the locking side of the Front door.
- C/D pillars- C-Pillar is the Rear most support to roof in case of a two row seats car, OR third support to the roof. D-pillar is the forth support to the roof and usually on the rear side of quarter panel.
- Ring panel - Ring panel is a structure panel connecting the rear portion of the body to front, and constitutes a big part in side structure.
- Quarter panels- Quarter panel is rear most panel of a body side structure.
- Drip rails/Gutters- Drip rails/Gutters is an exposed channel applied to the roof over the side windows to direct water away from the windows and to cover structural welding.
Bodyside Outer-
- The outside panels provide the shape of the car body whereas the inner panels reinforce the shell of the body. The various curved shapes are given to outer panels to provide the strength to panels. It includes 'A,B,C and D'-Pillars, quarter panel,sill area,etc.
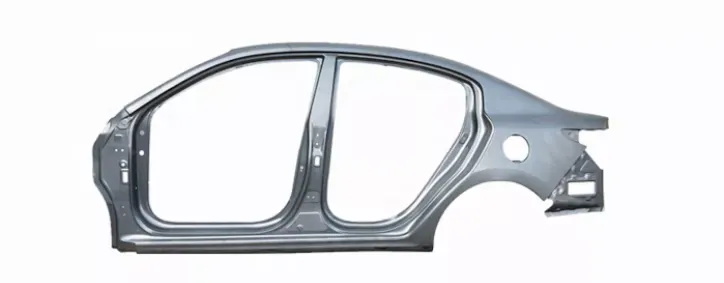
Bodyside Inner-
- The inner panel provides mounting locations for various trim panels and connecting assemblies. These two panels are welded together to pillars and rails so as to form the skeleton of the car body.
Underbody
Front End Under Frame (Engine compartment)-
It is an engine compartment area where all possible mounts for engine and other components get fixed.
- PLENUM Panel - Plenum is a chamber located between the throttle body and the runners of the intake manifold, used to distribute the intake charge evenly and enhance engine breathing.
- FRT wheel house/ Fender - FRT Wheel house or Fender is an encasement around the FRT wheel.
- Wing panel - Wing panel are the outer most side panel in the front.
- Cowl - Cowl is the portion of the body bounded by the front fenders, the base of the windshield, and the rear edge of the hood
- Upper tie bar- Upper tie bar is the upper panel in front connecting the two sides (RH/LH) of Front structure.
- Lower tie bar- Lower tie bar is the lower panel in front connecting the two sides (RH/LH) of Front structure.
Main Floor-
It is an area where transmission, instrumental panel or dashboard, seats and other components will fixed.
- Dash panel - Dash panel provides a partition between engine and the driver/passenger cabin inside car
- FRT Floor - provides a base for seats mounting and provides partition between transmission /propeller shaft/ground and the cabin.
- Riser connects Front floor to Rear Floor by providing a level difference
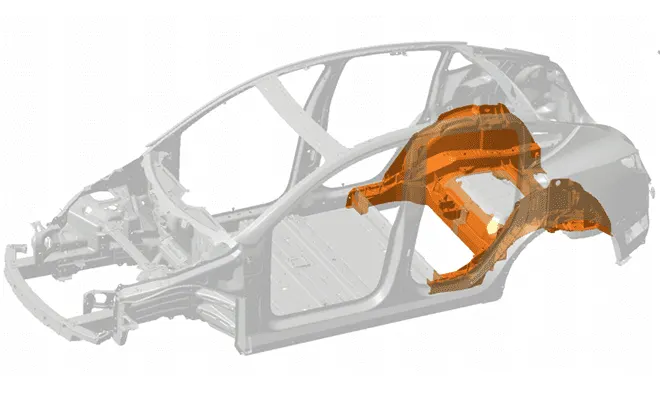
Rear End Under frame (Rear compartment)-
It is an area where spare wheel or stepheny will be placed as well as other components and will have boot space.
- Rear Floor- Rear Floor is the floor on the Rear of the car and provides a partition from ground also provide base for Rear seat mounting.
- Rear wheel house
Closures
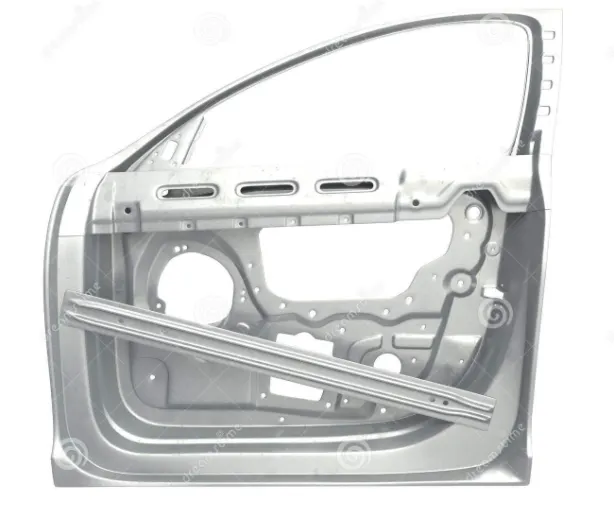
Front & Rear Door(Inner & Outer panel)-
These are side closures of cars to protect the passengers.
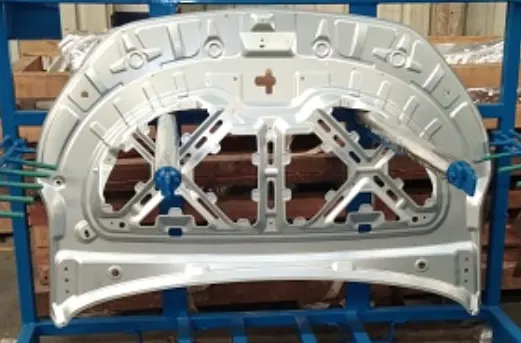
Hood-
Inner & Outer Panel-
It covers the engine compartment.
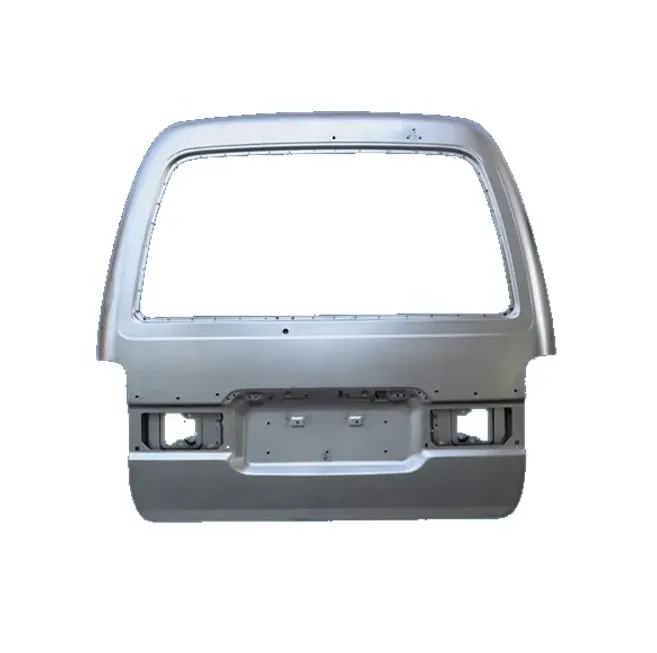
Decklid/Backdoor/Tailgate-
It covers the boot space or rear compartment of the car.
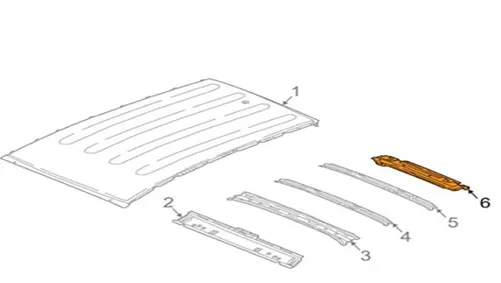
Roof-
Inner & Outer Panel-
It covers the top of the car to protect from different weather conditions.
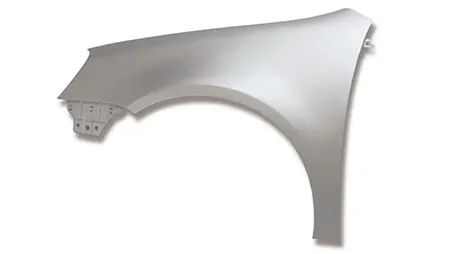
Fender-
It covers the top of the front wheels .
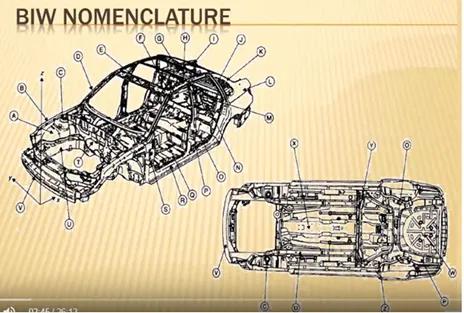
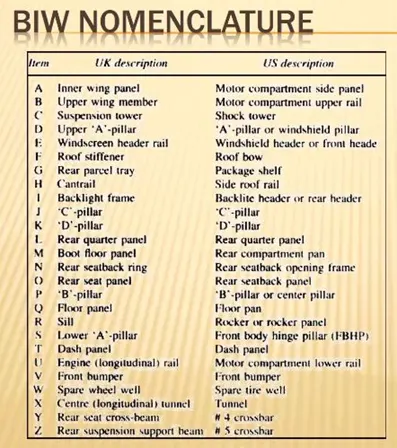
2. BIW nomenclature
- A nomenclature in BIW is basically naming every part of the body.
- These names can be said as subparts of the already categorized parts above.
- The nomenclature differs a little bit from region to region but the overall idea is to name individual automotive sheet metal components.
- The terms are standard but they differ in some countries.
- As automotive industries spread worldwide, the terms and standards will be different for similar components.
- For example, One component of BIW is known as inner wing panel in the UK description another side the same component of BIW is known as the Motor compartment side panel in the US description.
3. Fixture
Fixture is a holding device which holds the workpiece to be processed. In general fixtures are designed using 3-2-1 principle. Further, fixture should firmly hold the work piece without causing vibrations, distortions, stresses in the workpiece and also fixture should not disturb or interfere the processing of the workpiece.
Types of fixture:
- Production fixture
These fixtures are used for mass production. Since these fixtures are used for mass production, they should be simple, rigid and hard. These fixtures should be periodically maintained in regular intervals to avoid errors and repairs. The design of the fixture should be in such a way that it should be easy to load and unload the workpiece within seconds to increase the productivity of the processing/assembly.
- Pre production operation fixture
These fixtures are basically newly designed fixtures for the new products or parts. These may be complex, manual and heavy based on the application. These can be referred as the protype fixtures. Once the preproduction operation fixture functions properly, then modifications are made to improve and to make it simple and reliable. These fixtures are used in special cases or during initial or trail stages of processing/production
- Checking fixture
These fixtures are used for checking and inspection purpose. No processing is done in these fixtures. These fixtures consist of gauges for checking the dimensions and tolerances and its accuracies. In some checking fixtures, fixtures are fixed and CMM devices check the geometrical accuracies.
4. Principle of fixture design
The fixture is designed based on how the workpiece is fixed on the fixture. All the Degrees of Freedom of the workpiece are to be constraint.
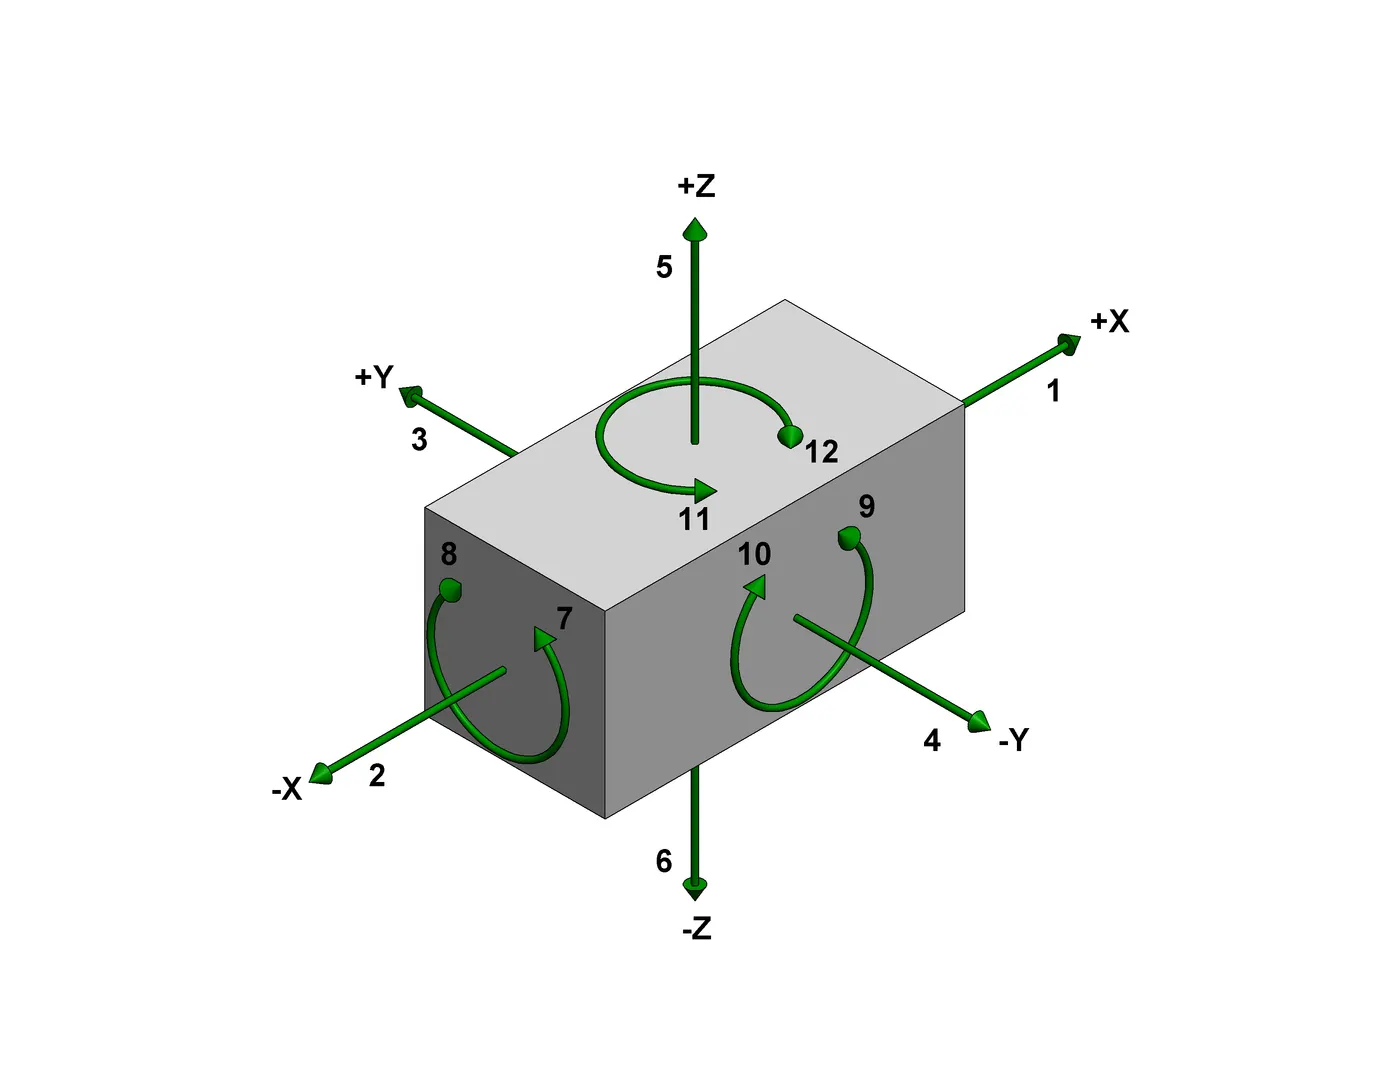
Those are:- 6 translational degrees of freedom +X, -X, +Y, -Y, +Z, -Z
6 rotational degrees of freedom-
- Clockwise around X-axis (CROT-X)
- Anticlockwise around X-axis (ACROT-X)
- Clockwise around Y-axis (CROT-Y)
- Anticlockwise around Y-axis (ACROT-Y)
- Clockwise around Z-axis (CROT-Z)
- Anticlockwise around Z-axis (ACROT-Z)
To make sure the proper fixing of the part we need to restrict all 12 degrees of freedom of the workpiece.
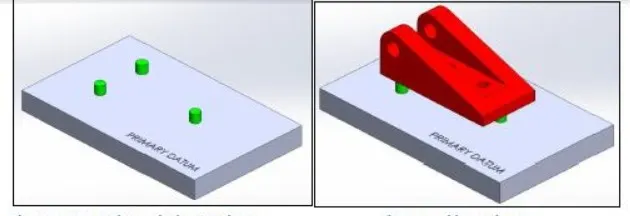
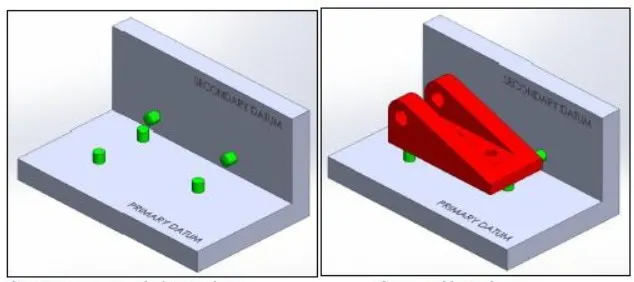
PRIMARY LOCATOR-
First, the three locators or supports are placed under the workpiece. It will be positioned on the primary locating surface also known as a datum. It will restrict 5 degrees of freedom.
SECONDARY LOCATOR-
The next two locators are normally placed on the secondary surface, restricting an additional 3 degrees of freedom.
TERTIARY LOCATOR-
This locator is positioned at the end of the part. It restricts 1 degree of freedom
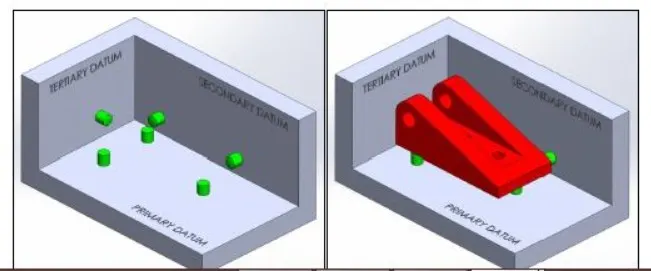
- All these 6 locators will restrict a total of 9 degrees of freedom. The remaining 3 degrees of freedom ( 1, 4 & 5 ) will be restricted by the clamps.
- To minimize the time consumption in assembly and disassembly, Have to use minimum numbers of pins to arrest a maximum number of degrees of freedom.
- The jig and fixture are tools used for holding the workpiece in a correct location for mass production. Various types of fixtures (like drilling fixtures, milling fixtures, and welding fixtures) are used in industry. The 3-2-1 method is the fundamental principle for all types of fixture design.
5. Types of BIW Stations
BIW Station is the part of BIW assembly line. The BIW assembly line is divided into zones and these zones are divided into stations.
The BIW stations are further divided into following-
- Tool stations
- Gripper stations
- Stand stations
- Miscellaneous stations
Tool Stations
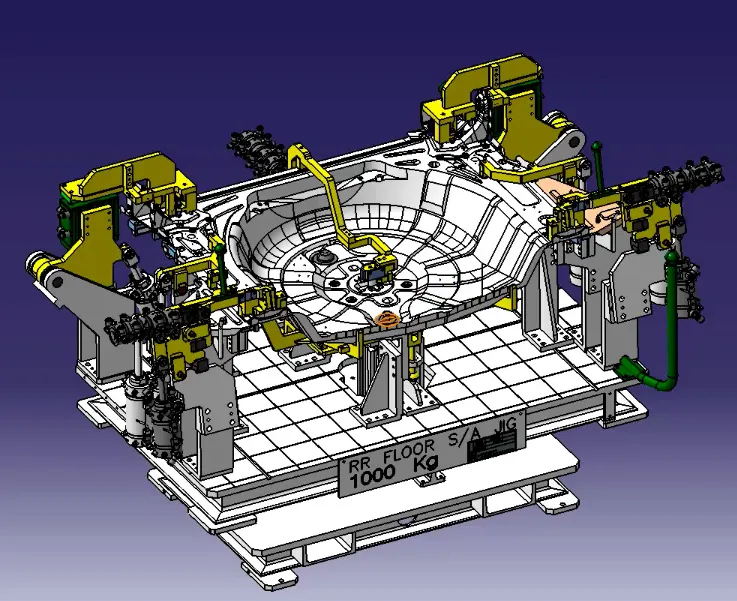
1) Geo Fixtures-
- A Geo tool is a fixture in which the geometry of the panels which are welded together is defined accurately. The pin tolerence for a geo pin will be closer tolerence, i.e. -0.15 in general. For example- Consider panel hole size 20 mm, the pin diameter should be 19.85 mm.
- In Geo fixture spots/ MIG welding done in such sequence that after taking out from the fixture it achieve the desired accuracy and doesn’t get disturb during transportation from Geo fixture to re-spot fixture. Geo fixture control the sub assembly accuracy in all the 3 axis.
2) Re-spot Fixtures-
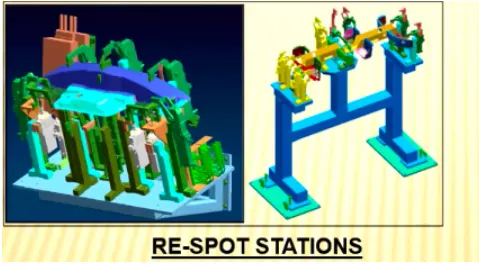
- A re-spot fixture/tool is a fixture in which the remaining weld spots which are not achieved in geo tool are welded for the pre welded panel from the geo tool.
- The Pin tolerence for a re-spot pin will be of tolerence with -0.28 in general.
- For example- Conside panel hole size 20 mm, the pin diameter should be 19.72 mm.
3) Marriage/Hemming Fixture-
- A marriage or a hemming tool is a fixture in which the inner panel assembly and outer panel aseembly are joined together.
- These are done by welding or hemming (in case of closure panels).
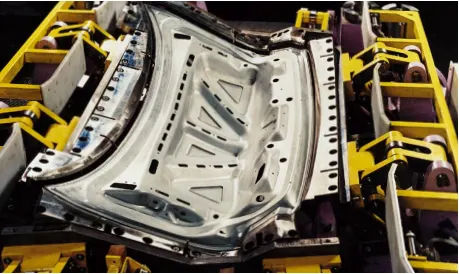
4) Checking Fixture
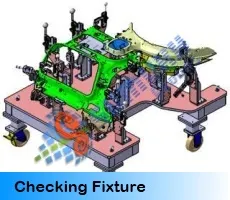
- These are used to check the assembly of parts, Tolerance, Dimensions &
- It can be of gauge type, Fixed type of automated checking.
- A checking gauge is a tool where the workpiece is held & different measuring gauges are introduced to ensure dimensions & repeatability.
- A fixed type checking fixture is used where the workpiece is fixed with clamps & pins & CMM is used which measures the coordinates of the different points of the panel or Then is compares with the CAD data & gives a report.
Grippers Stations
A gripper is a device that enables the holding of an object to be manipulated. The easier way to describe a gripper is to think of the human hand. Just like a hand, a gripper enables the holding, tightening, handling, and releasing of an object. A gripper is just one component of an automated system. A gripper can be attached to a robot or it can be part of a fixed automation system. Also known as EOAT (End Of Arm Tooling).
Different grippers are used in BIW as follows-
- Material handling gripper
- Process grippers
- Combo Gripper
- Dual Gripper
Stands Stations
Stands are used to hold the part when not in use or also it is used to mount some parts or bodies on it.
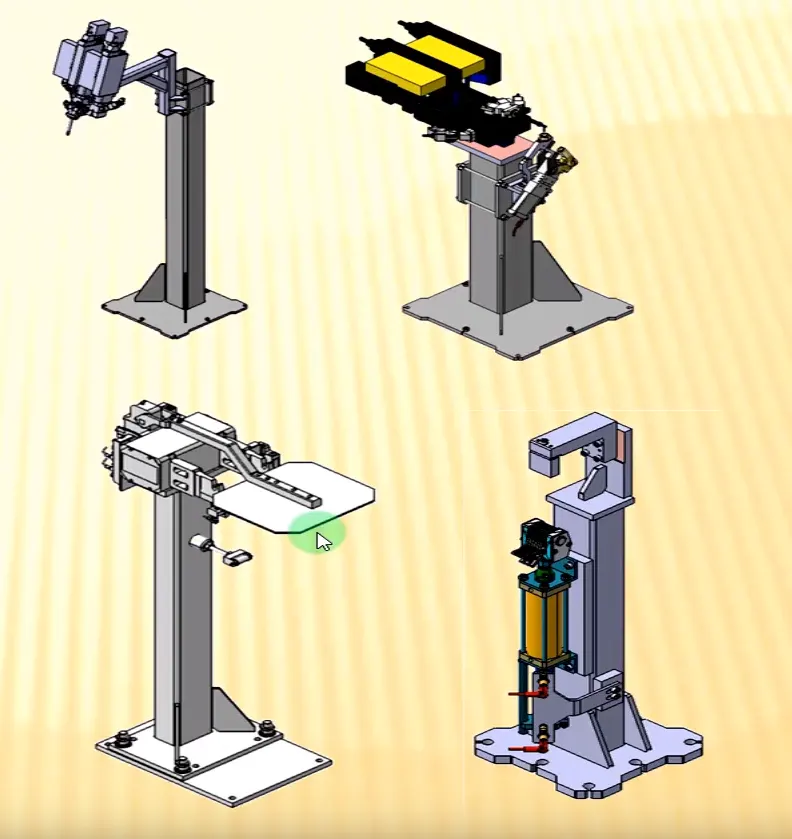
Different stands are used in BIW-
- Pedestal stand
- Gluing & sealer stand
- Docking stand
- Date stamp stand
Miscellaneous stand
A) Curing
- After gluing it needs some time to cool down, so we put the assembly on some belts & it will take the panel to another station & meanwhile gluing will cool down.
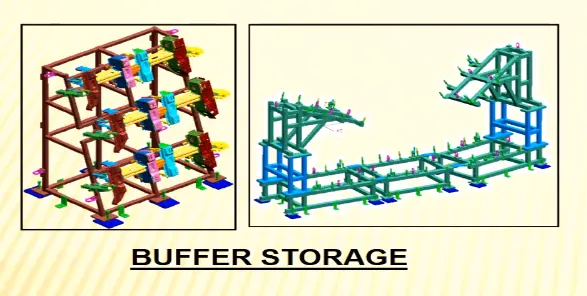
B) Buffer stand
- After some operation, we can put the no. of assemblies in this stand which is buffer stock & it can be transported to another station in easily. They are also used to store the inventory while the machine is undergoing some maintenance.
C) Take out trolleys
- It used to take out some panels for inspection to rectify the process is going in the right or not, between the cycle.
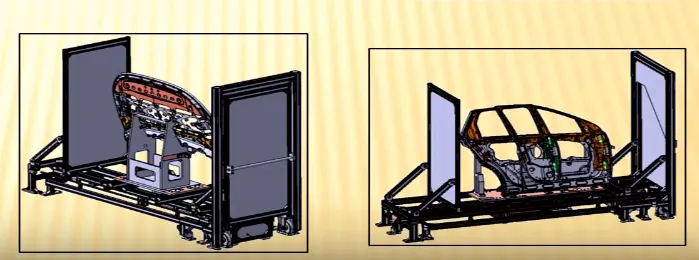
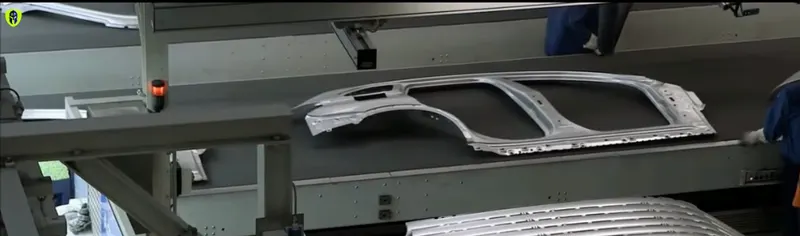
D) Conveyor
- The conveyor is the rotating moving path that transports the parts to the next station which are kept over it.
5. Basic terminologies used in the BIW fixture
The terminologies used in BIW are;
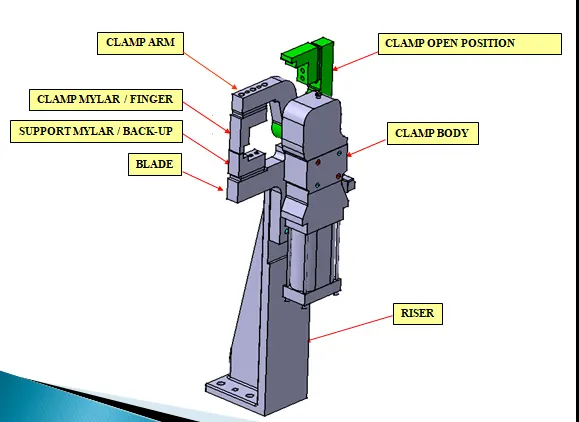
NC/Mylars/Fingers
- Mylars are the component that holds the panel while these are placed from topside & from the bottom side also. The top side Mylars called Clamping Mylars & the bottom side Mylars called Resting Mylars. Every clamping Mylars have resting Mylars. It doesn't allow deformation of the part due to welding stresses.
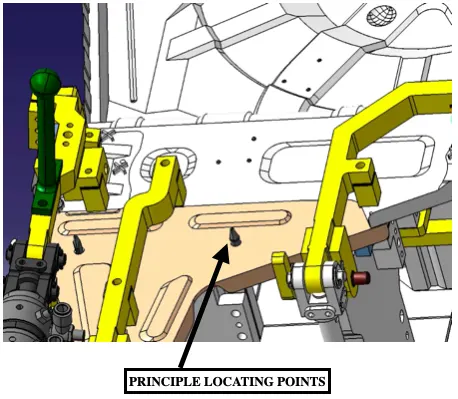
Principle locating point (PLP)
- These are used to accurately locate the workpiece on the fixture to process the workpiece.
Blade
- Blades are the plates which are attached to the risers.
Risers
- Risers are of different types like L-typer rises, welded, Square tube riser. Riser is the manufacturing part which gives height to the assemblies.
Shims
- Shims are the small part that comes with the thickness of 0.1mm, 0.2mm, 0.5mm, etc. These will compensate for the stackup tolerance which reflects at the panel holding part. We give tolerance to all the parts of the fixture. Due to this tolerance, the Mylars will either lift up or goes down from their defined position.
- If the Mylars go down from the defined height it will make an impression or dent on the panel.
- If the Mylars lift up then there will be a distorsion due to welding stress. To adjust the Mylars at its defined position we use shims so the panel won't be deformed & also don't get any impression on it.
Rough locators
- The operator can place the part in the wrong orientation. The rough locator will work as a guide while placing the part in the fixture & the part will be loaded in the exact orientation.
Hardware
- Hardware are the Hex head bolts, Allen Bolts, Hex nuts, Spring washers, Self-locking nuts.
Units
- The fixture is the assembly of different types of units. There are different units like pin unit, base unit, clamping unit, etc. which makes a complete assembly.
Number plates
- The number plate is the aluminum embossed plate placed on each unit for easily recognizing the unit.
Co-ordinate Plates
- Every fixture has a tooling hole through which all fixture checked. Co-ordinate plates are used to cover the hole.
Nameplate
- The data like manufacturing company name, fixture type, Fixture weight is embossed on the plate and joined to the fixture.
Clamp Arm
- The clamp arm is the part of the clamp unit which moves with the (Mylars mounted on it to hold the assembly).
Pivot
- It is an axis about which the clamp arm will rotate or move.
Class A Surface/Skin surface
- The outer panels of the car like a hood, door, backdoor, fender, roof are visible to the customer. Those outer panels should be aesthetically very good. No scratches or dent is acceptable over it.
- While designing the fixture for the skin surface the clamping material should be soft, so that it could not be able to left any impression or dent over the skin. Generally, nylon or PU material is used for clamping purposes.
Reed switches & sensors
- These are the electric components, the reed switch and sensors are only used in automated fixture. They detects that panel is loaded or not on the fixture assembly.