Hood design-Week 2
HOOD DESIGN
AIM:-
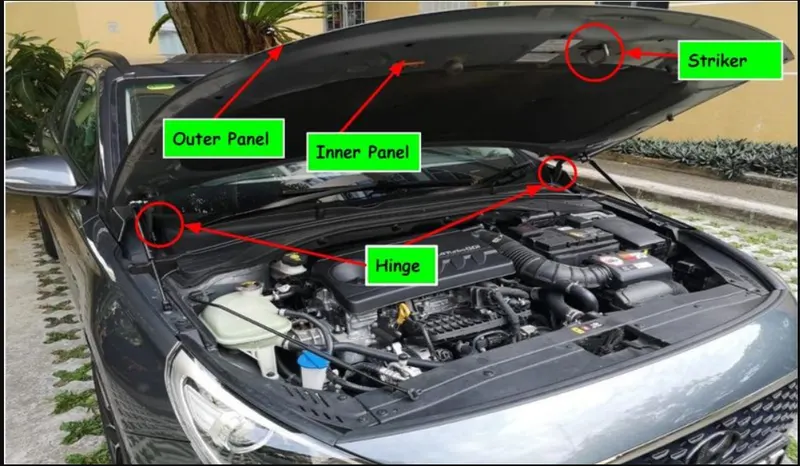
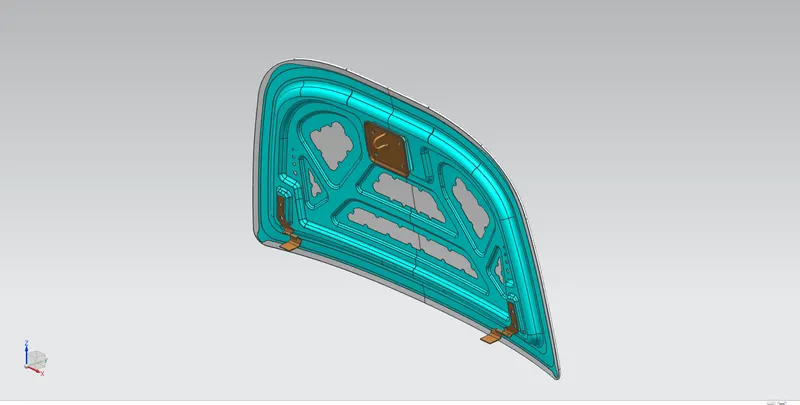
In this project, a Hood Assembly will be designed which would be consists of a hood outer panel, hood inner panel. The latch for the hood will also be placed at an appropriate position considering that the hood should be opened and closed easily using its mechanism. The hinges will also be placed at the appropriate position for the rotation of the hood inner panel.
INTRODUCTION:-
The hood or bonnet is the hinged cover over the engine of the vehicle. Hoods can open to allow access to the engine compartment or trunk on rear-engine and some mid-engine vehicles) for maintenance and repair.
A car hood is meant to protect the performance parts of your vehicle, including the engine, while also providing easy access for repairs and maintenance. The hood can incur damage as well. One of the most common types of damage is to the hinge, which is the device that connects the hood to the body of the vehicle. Over time, the hinge can become loose or may fall off completely. The hood is also prone to receiving scratches and dents. Although this might appear to be a minor problem, dents and scratches can lead to depreciation in the value of your vehicle. Scratches and dents can also lead to exposure to the elements that can result in rust and corrosion. This can be a serious problem that can ultimately expose the engine in your car to snow, sunlight, and rain. When this happens, it can impact the performance of your car's engine.
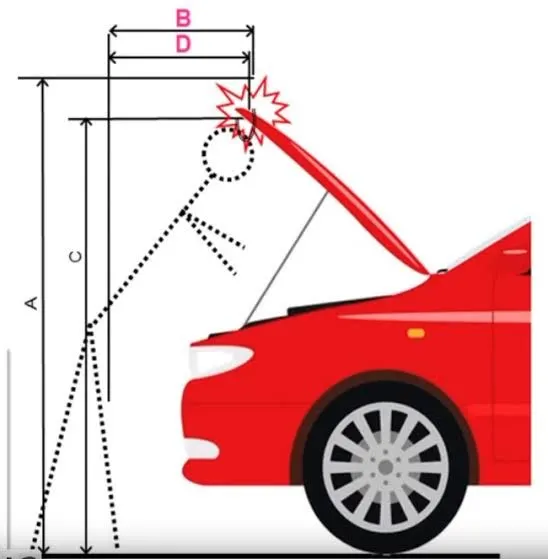
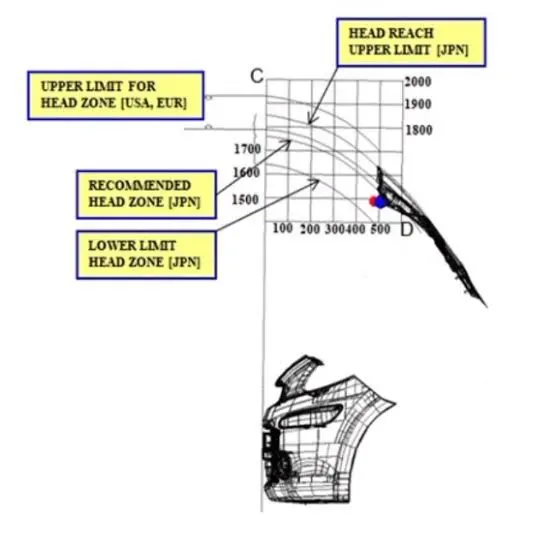
The first important criterion for designing the hood is to set an opening angle till which the hood panel can be opened. This opening angle is different for different countries which largely depends on the average height of that particular country. person in that particular country.
The movement of the hood can be controlled by either one of them:
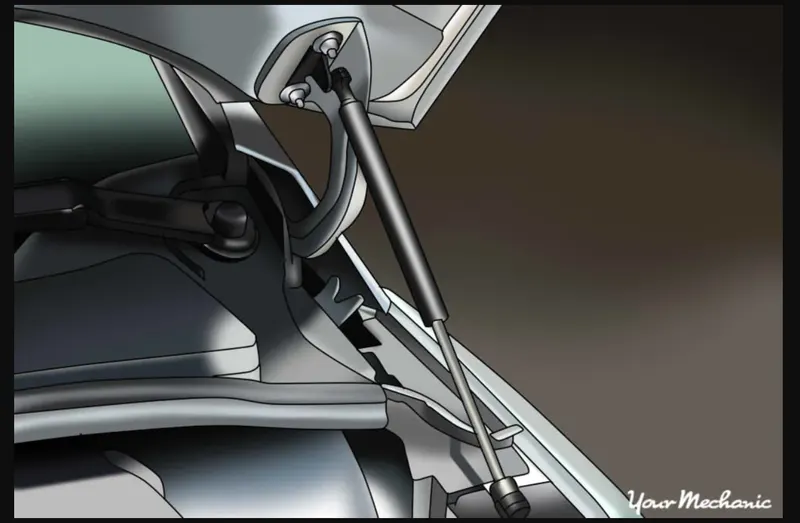
1. Gas stay
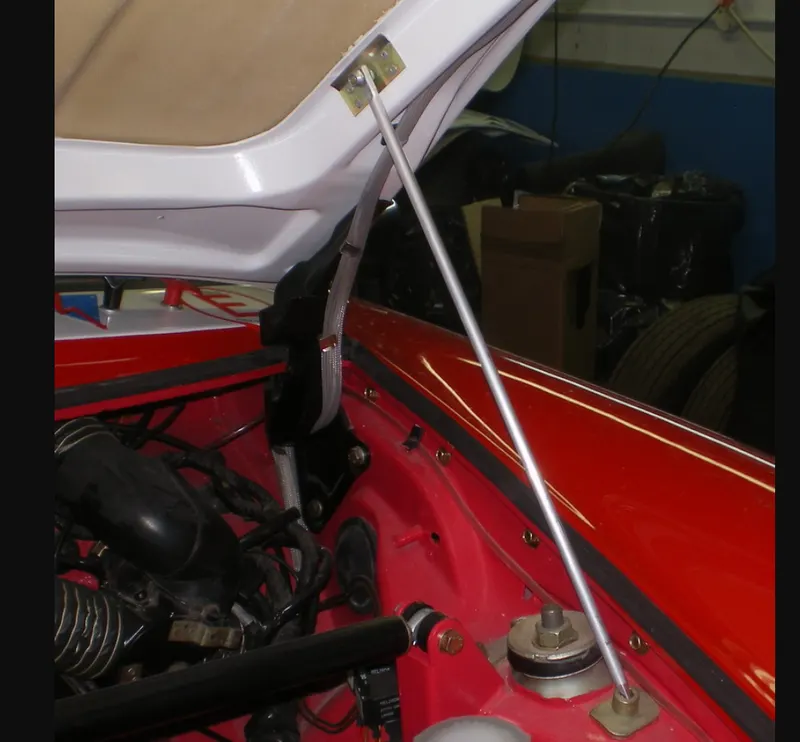
2. Support rod
1. Gas Stay:-
A gas stay is a type of spring that, unlike a typical mechanical spring that relies on elastic deformation, uses compressed gas contained within an enclosed cylinder sealed by a sliding piston to pneumatically store potential energy and withstand the external force applied parallel to the direction of the piston shaft.
2. Support Rod:-
This is the most commonly used rod for opening and closing the hood at a certain angle. One end of the rod is hinged to the engine compartment and the other end is set free so that it can be locked to the hood inner panel when the hood is opened. This is usually used when the weight of the bonnet is small.
It is very important to consider that the support rod should not collide inside the engine compartment.
Pedestrian safety NCAP (New car assessment program) standards:
Globally, various NCAPS are present that carry on the pedestrian safety tests on new vehicles and rate them accordingly.
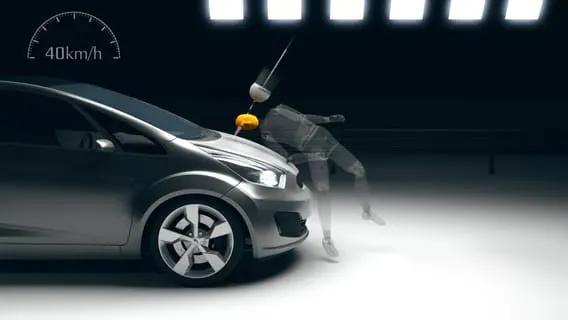
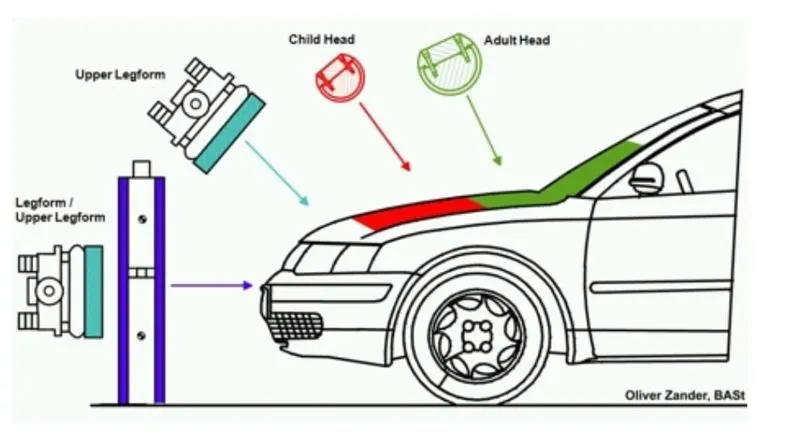
1. Head Impact:-
This test is carried out for a vehicle speed of 40 km/h. To have an estimate of the potential head injury in the fateful event of a vehicle striking an adult or a child, a head form impactor is used in a series of impact tests, and the impact sites are then assessed for and rated accordingly. This test will give essential information about the
deformation clearance, energy-absorbing structures, and deployable protection systems such as pop-up bonnets and external airbags in a new vehicle.
2. Upper Leg Impact
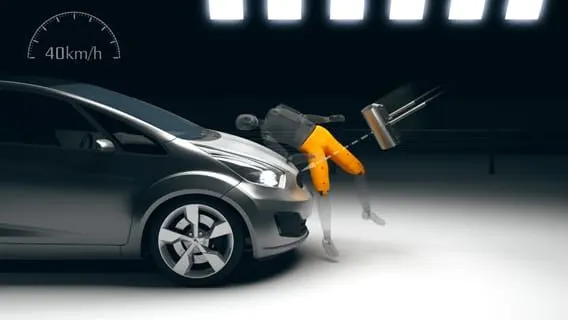
The facility carries out the test at a vehicle speed of 40 km/h. An adult upper leg form impactor is used in a series of impact tests and then the impact sites are assessed. The protection is then rated as good, adequate, marginal, weak, or poor. The test procedure allows to check the energy-absorbing capacity of the structures of a vehicle and also check whether the geometry of the vehicle allows mitigation of injuries.
3. Lower Leg impact
Euro NCAP carries the test at the same speed standard as the above ones. It uses an adult leg impactor and a series of tests are carried out. Impact sites are then assessed and the protection rating is offered.
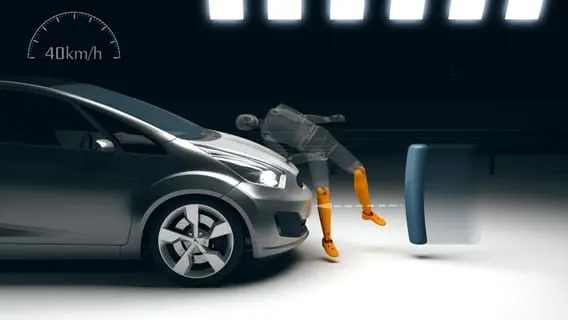
For this test, Euro NCAP uses a specially designed cyclist form that will replicate the actual cyclist on the road. Euro NCAP offers the highest rating if the collision is completely avoided. The vehicle is also awarded if the speed is reduced as any reduction in speed of impact can significantly reduce the injury to the vulnerable user.
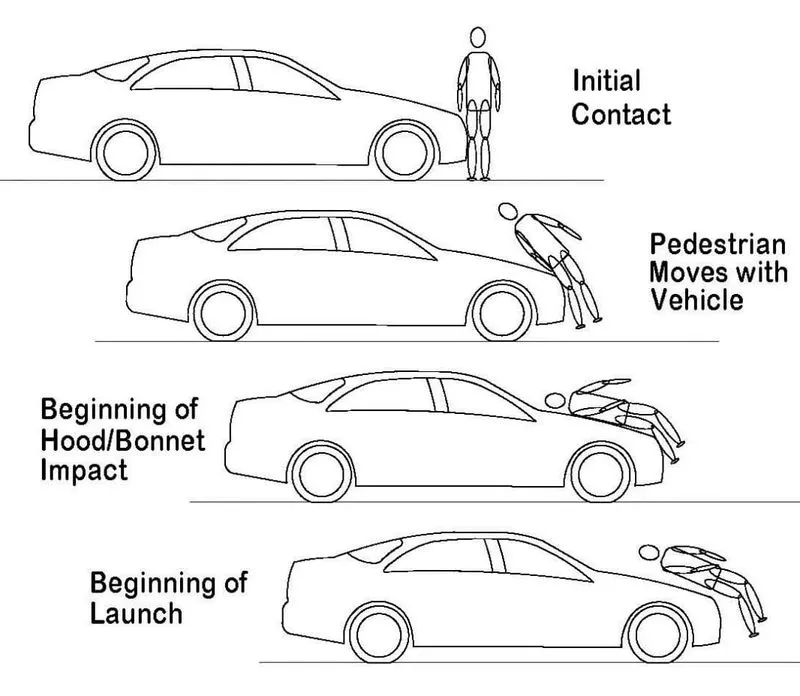
To measure the potential head and leg injuries in the front portion of the car illustration of crash mitigation tests are designed below:
NVH (Noice, Vibration, and Harness)
Noise, Vibration, and Harshness, and is a measure of how much unpleasant aural and tactile feedback the car delivers as you drive.
What does NVH mean?
The noise is what you can hear, the vibration is what you can feel and the harshness is how much of an effect thumps, bumps, noise, and vibration have on the cabin and its occupants. Removing and isolating passengers from NVH is a field that's seen monumental advances over the past few decades. Originally the preserve of the most luxurious marques - and an acronym that was only even discussed by premium brands -NVH reduction is a global push, spurred on by consumers who want increasing insulation from the environment they're driving through
What causes NVH?
Noise, vibration, and harshness are caused by the car's mechanical and electrical systems, as well as the car's interaction with road surfaces and its passage through the air. The main sources of NVH in a car are its engine. drivetrain and tires, as well as the sound of airflow along its body.
Tires are a huge source of noise, due to vibrations created by their rotation, which then travel along with suspension mounts and into the cabin Low-profile tires, found on sportier cars, tend to transmit more vibration through the suspension because the tighter, stiffer rubber can't absorb as much. Wide tires are more susceptible due to a larger contact patch, but the soft, wide tread patterns of off-road tires are the worst offenders.
Airflow over the car's body causes quite a bit of noise, especially at higher speeds and in large cars with the aerodynamic properties of a shipping container. Any interruptions the air faces in its journey across the car-such as aerials, roof racks, and door mirrors-are rewarded with howling, whipping, or buzzing noises in the cabin.
How to reduce NVH?
Canceling out NVH comes down to three basic principles-reducing it at the source, isolating it from the car's main structure, and absorbing as much as possible before it enters the cabin. The first-if, not the easiest way to reduce NVH is to curb the number and volume of the sounds, vibrations, and shocks produced in the first place.
The second and perhaps equally complex way to reduce NVH is to isolate the car's main structure from the source. Complex and expensive suspension tech such as independent, multi-link, and hydro-pneumatic systems isolate the chassis and steering column from road surfaces removing vibration and shocks.
To further isolate the sources of noise, the engine. suspension and exhaust components are mounted on rubber and polyurethane bushes rather than solid metal the softer compounds work against the transmission of vibrations
The last resort in the war against NVH is also the most conventional absorbing as much as possible Mechanically speaking, this tends to refer to steering dampers, which absorb the worst of the shocks introduced by poor road surfaces.
Design of the HOOD using nx software:-
Input Data
1. Outer hood panel thickness = 0.75mm
2. Inner hood panel thickness = 0.75mm
3. Reinforcement thickness = 1.5mm
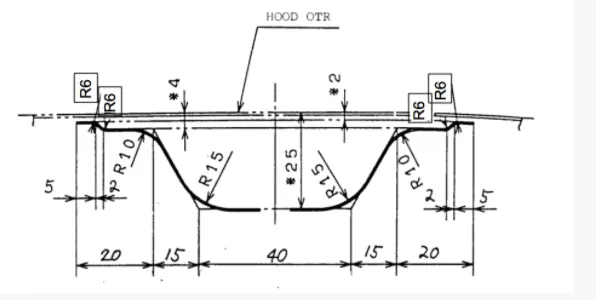
The master sketch that should be used to design the outer and inner panels is shown below.
Hood outer panel:-
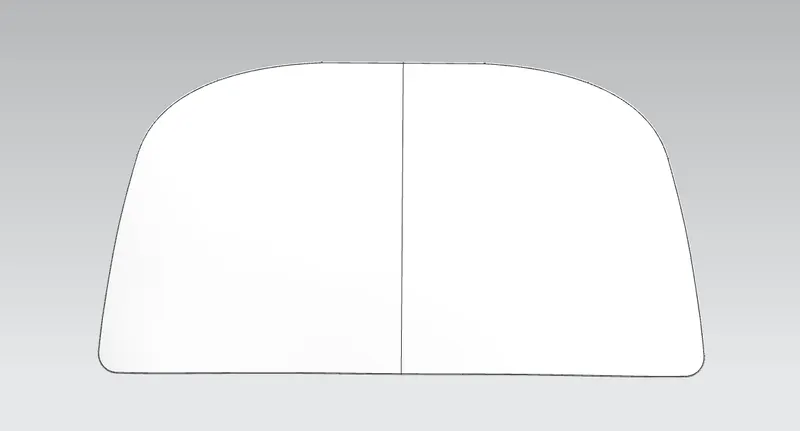
Outer panels are the aesthetic elements of a car. It is the styling team that provides the skin for the outer panel. The shape, position, and size of the hood should satisfy the safety norms. So while designing the hood we should give more importance to pedestrian safety. The outer panel is attached to the inner panel by hemming.
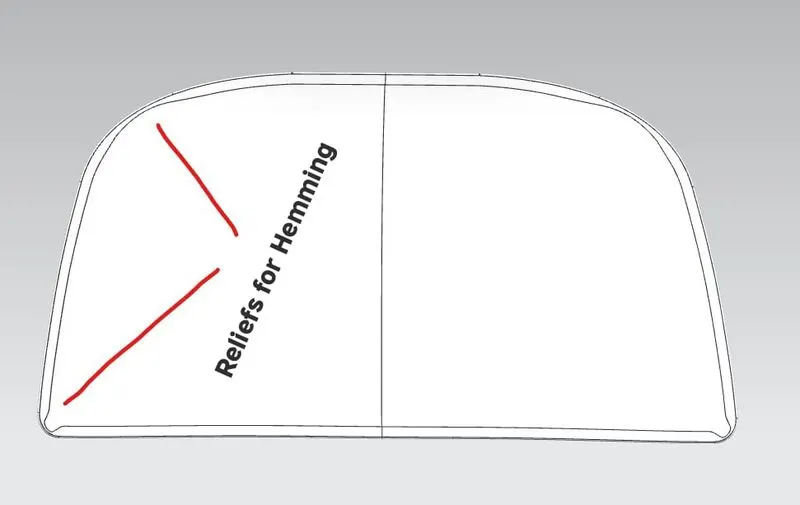
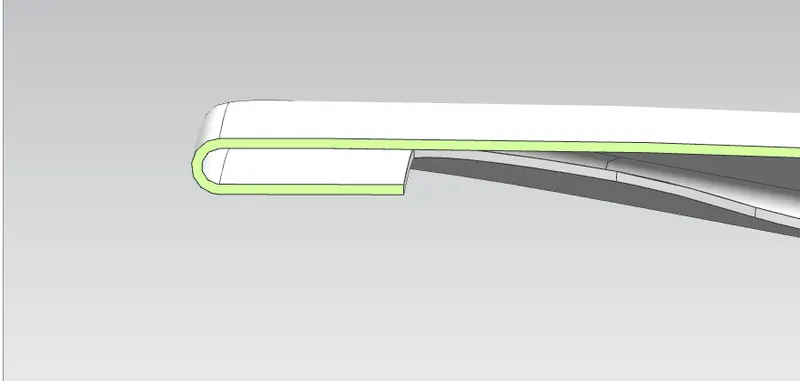
So, it is necessary to provide the required hemming flange and reliefs for the hemming operation. We also provide mastic sealants between the outer panel and inner panel to reduce vibration.
Hood inner panel:-
The inner panel of the hood acts as a reinforcement for the hood outer panel which provides strength to the outer panel. The thickness of the hood inner panel is 0.75 mm. To reduce cost and increase the strength of the inner panel embosses are made on the sheet metal along with the cutouts.
Emboss
Sheet metal embossing is a stamping process for producing raised or sunken designs or relief in sheet metal. This process can be made using matched male and female roller dies, or bypassing sheet, or a strip of metal between rolls of the desired pattern. It is often combined with foil stamping to create a shiny, 3D effect.
The metal sheet embossing operation is commonly accomplished with a combination of heat and pressure on the sheet metal, depending on what type of embossing is required. Theoretically, with any of these procedures, the metal thickness is changed in its composition.
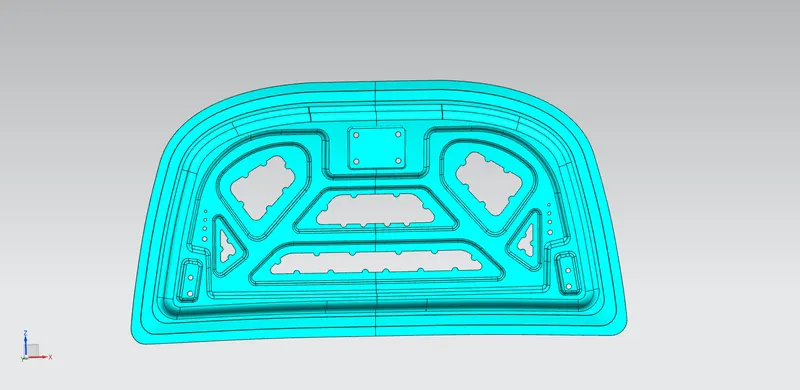
The metal sheet is drawn through the male and female roller dies, producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet. The pressure and a combination of heat actually "irons" while raising the level of the image higher than the substrate to make it smooth. The term "impressing" refers to an image lowered into the surface of a material, in distinction to an image raised out of the surface of a material.
In most pressure embossing operation machines, the upper roll blocks are stationary, while the bottom roll blocks are movable. The pressure with which the bottom roll is raised is referred to as the tonnage capacity.
Reinforcement for latch and hinges:-
The material that strengthens the existing material when added to it is called reinforced material. As the latch and the hinges will be placed on the embosses so that strength at this position will be less and that portion can get easily damaged due to movements.
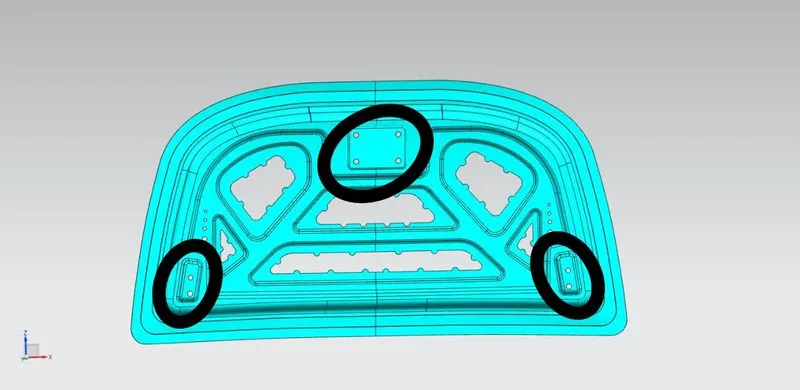
To provide strength at these places a 1.5 mm, thickness reinforcements will be placed. Reinforcement will be a metal part spot-welded into the emboss of the hinge and the striker. It can't be seen from the outside as it will be welded in the back portion of the hood inner panel.
Latch Trajectory
The latch should be placed at the appropriate position so that it does not become an obstacle while the hood is opened and closed. For this purpose, it should be placed perpendicular to the hook.
To achieve the above condition a line will be made using the axis of the hinges on the opposite ends. About the midpoint of this line, a datum plane will be made and then a sketch will be on this datum plane.
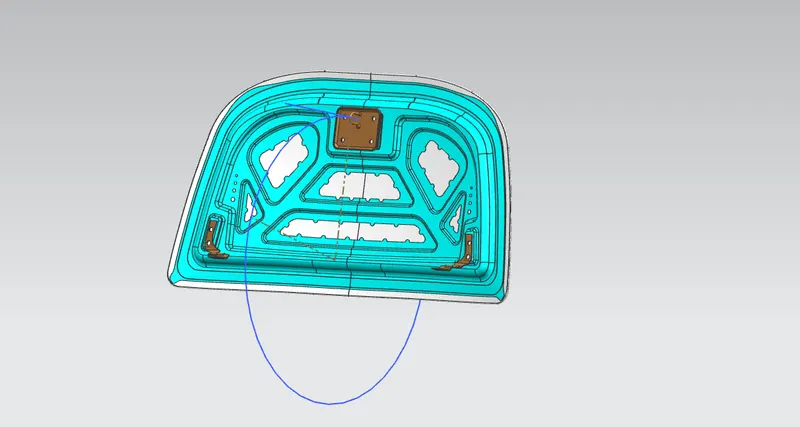
Inside the sketch, a circle will be made which will indicate the trajectory of the opening and closing of the hood, and then a line will be made which will exactly position the latch at the appropriate position.
A tangent line will be made on the circle which will touch with the previous line. Another straight line will be sketched on the latch which would be perpendicular to the latch.
Now both the straight lines will be coincided with each other using the align feature in the assembly workbench. By doing this the latch will get arrested perpendicularly and will follow the circular patch so that the hood can be easily opened and closed.
Mastic Data
Hood commonly possesses a large surface area and hemming can only be provided through its boundary. We cannot use other joining techniques like welding, riveting, etc because they leave marks on the outer panel which spoils its aesthetic appearance. So, mastic sealants are used to stick the inner surfaces of the outer panel and inner panel. Mastic sealants are elastic compounds that behave like rubber. It is applied between the inner and outer panels at specified spots. Each spot of mastic sealants has its effect around a circular region of 80mm diameter. Thus, the mastic points are arranged in such a way that it covers the areas away from the hemming which is more vulnerable to vibrate.
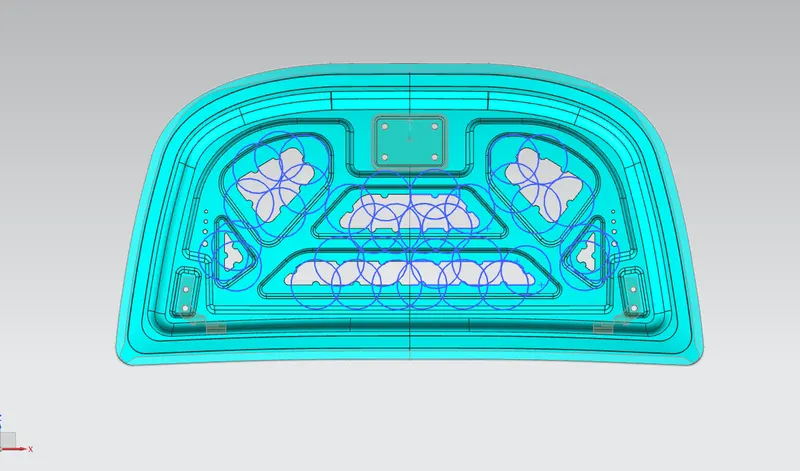
The assembly of the hood inner and outer panel is shown below:-
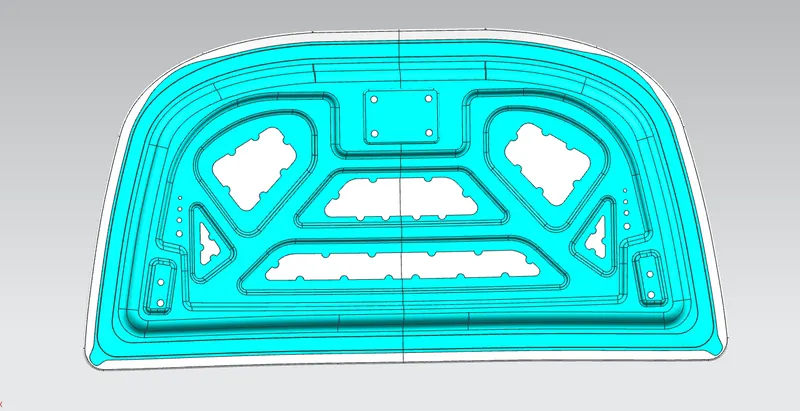
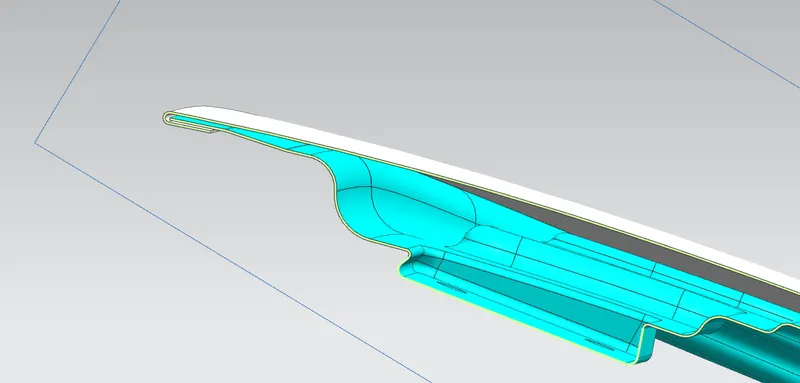
The manufacturing process involved in making different features of the sheet metal
What is Deep Drawing?
Deep drawing is the process of converting blank sheet metal into cylindrical containers with a flat or hemispherical base. It is a combination of metal forming process & sheet metal process If the ratio of height to diameter of the product is greater than 0.5 then this drawing operation is known as deep drawing.
- It consists of die, punch, blank holders.
- After the application of drawing force, the blank of material forms & takes shape of the punch or shape made onto the punch. To avoid frictional resistance between blank & die, lubricant is used.
- The applications of the deep drawing process are kitchen utensils, cylindrical containers, fire extinguishers
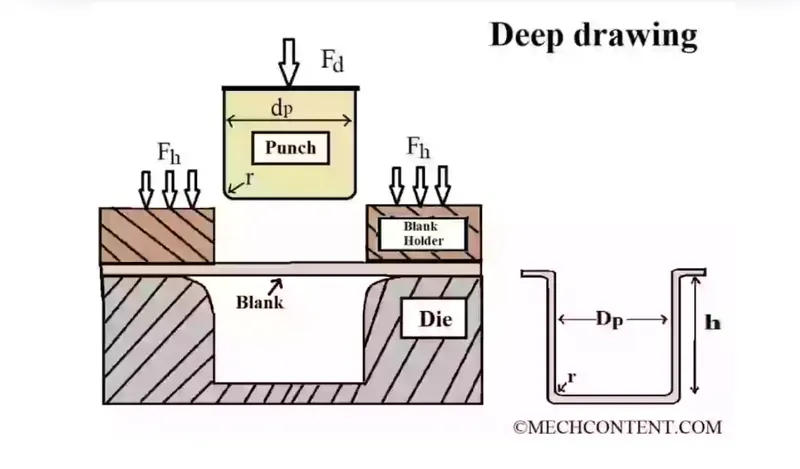
The Deep Drawing is shown above
The rigid tools consist of a punch, die, and binder. In deep drawing, the plate holder closes after the metal sheet blank has been inserted.
Next, the sheet is clamped between the die and the binder. This process slows down the flow of the sheet while it is being drawn and thereby prevents wrinkles from forming under the binder. The punch stretches the sheet over the die radius and forms it in the die. The amount of punch force necessary for forming is thereby continually increased up to the lower dead center of the punch.
Whereas in pure deep drawing there is no reduction of sheet metal thickness, forming is achieved in stretch forming purely as a result of a decrease in sheet metal thickness. Stretch forming is extensively used for the forming of only slightly curved parts with a low depth of draw (e.g. roofs, doors).
When drawing complex car body parts in practice, there is usually a combination of stretch and deep drawing involved. The sheet metal must be stretched as well as possible without reaching the material's limits
Hemming
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part to achieve a tight fit. Normally hemming operations are used to connect parts, to improve the appearance of a part, and to reinforce part edges.
In-car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming, and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids, and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas, or material roll-in. This is why it is important to use simulation tools to, on the one hand, better understand the hemming process and, on the other hand, significantly reduce the number of “trial and error” loops during tryout and production.
There are various types of hemming operations:
- Conventional die hemming
- Roll hemming
Conventional die hemming
Conventional die hemming is suitable for mass production. In die hemming, the flange is folded over the entire length with a hemming tool. Normally the actual hemming is a result of a farming operation in which the flange is formed with a hemming tool after the drawing and trimming operations have been completed. The formed flange is then hemmed in several process steps. These steps include, for example, the pre-hemming and final hemming depending on the respective opening angle of the flange. Production plants for conventional die hemming are very expensive, but the cycle times are very low.
Roll hemming
Roll hemming is carried out incrementally with a hemming roller. An industrial robot guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller that follows a defined path.
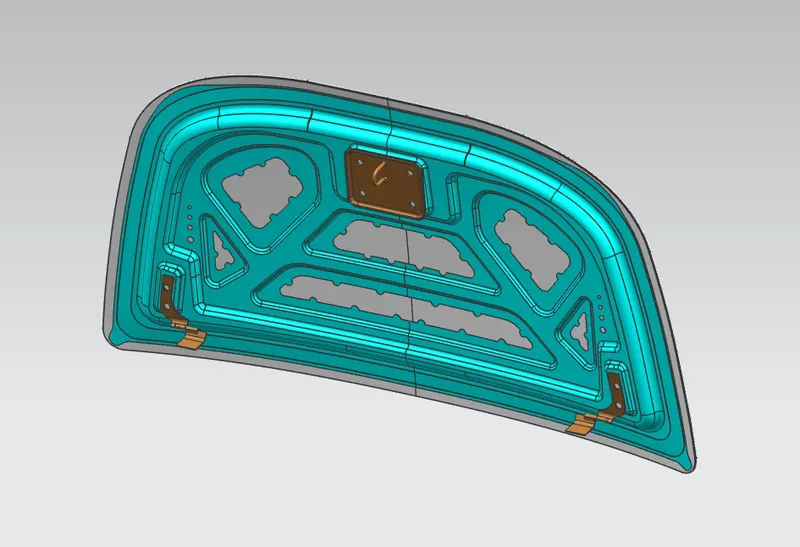
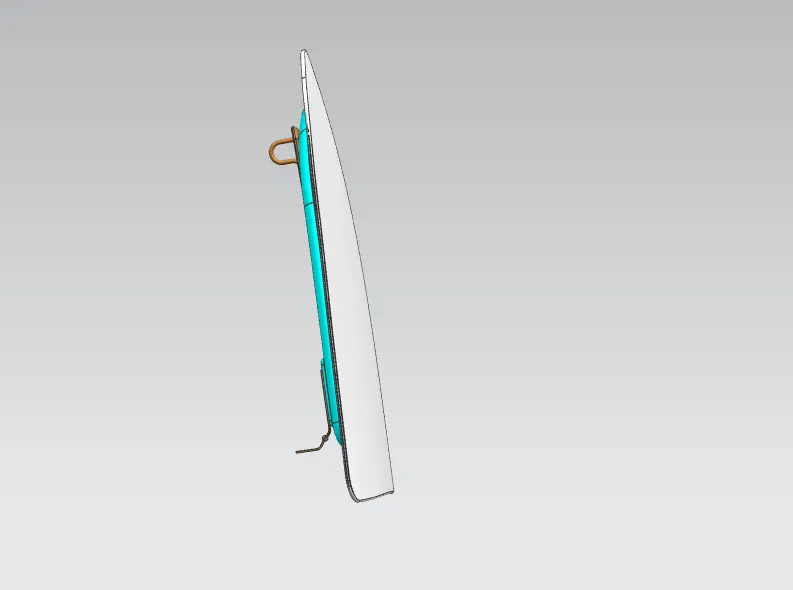
Final Hood assembly part.
Draft Analysis:
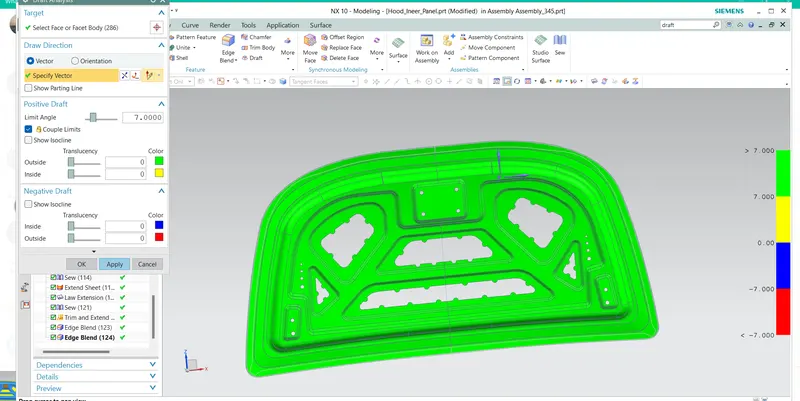
Draft analysis is useful in detecting the negative draft angle og the designed component. The draft angle is less than 7 degrees.
Conclusion:-
The Hood of the vehicle is designed considering the safety of passengers and pedestrians. The designed hood is assembled, Draft analysis is made as per the OEM standards.