Hood design-Week 2
Introduction:
Hood is the main component at the front portion of car. It is used to provide aesthetic look and add pedestrian safety. The shape of the Hood is made aerodynamic in order to minimize the air effect. Hood is generally used to access the parts easily such as radiator, engine and many other parts. A car hood, also referred to as a bonnet in some other countries, is the hinged cover that rests over the engine of a front-engine vehicle. Its purpose is to provide access to the engine for repair and maintenance. A concealed latch is typically used to hold down the hood. On vehicles with an aftermarket hood and on race cars, hood pins may be used to hold down the car hood. Hoods sometimes also contain a hood scoop, wiper jets, power bulge, and/or hood ornament. Car hoods are typically constructed from steel and sometimes from aluminium. Aftermarket car hoods may be constructed from various other materials, including carbon fiber, fiberglass, or dry carbon. The hood design may vary from one make and model to another.
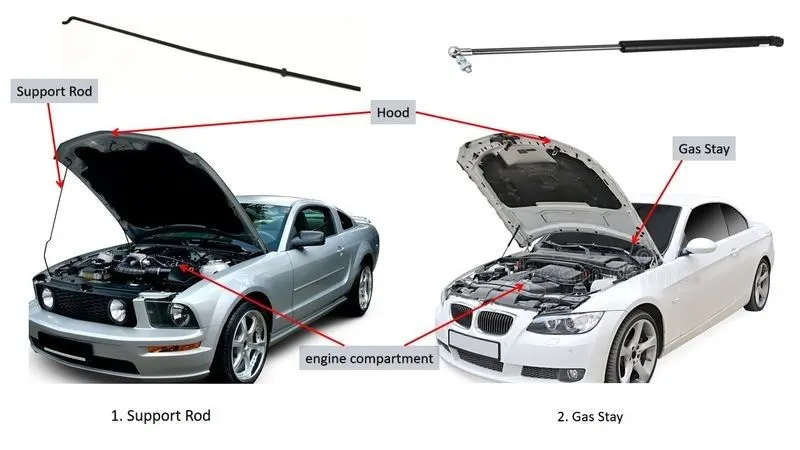
while access for repairs and maintenance Hood can fix by two methods
1.Support Rod 2. Gas Stay
Design requirements for Car Hood
- Hood Head zone for lock striker:
In the following figure Hood Head zone for lock striker
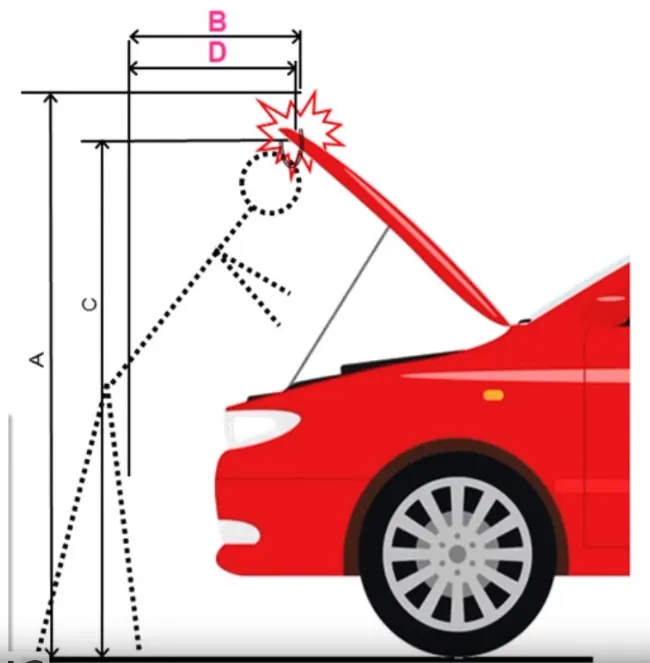
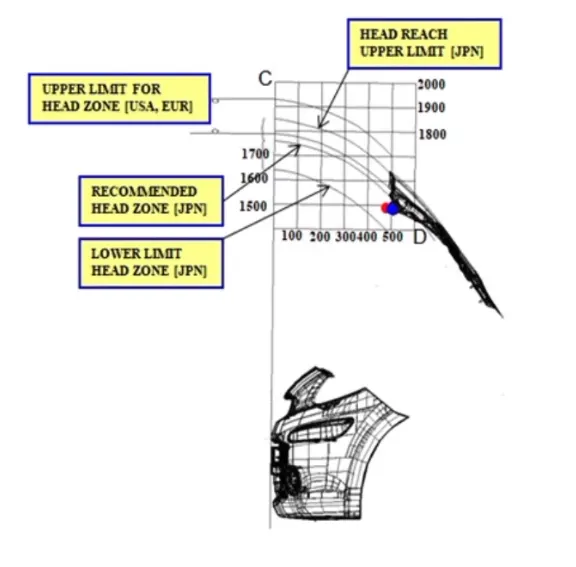
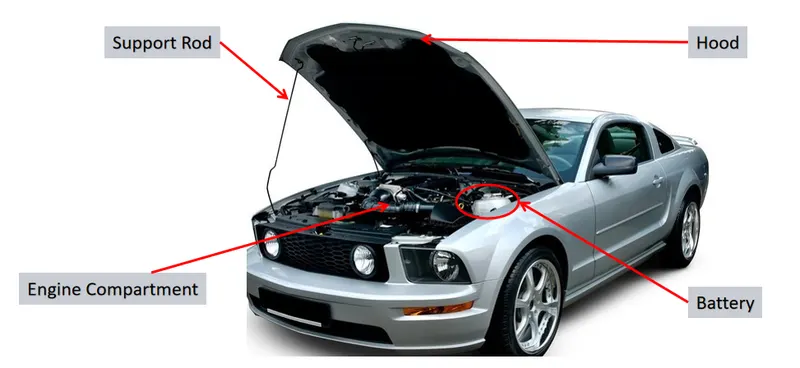
The opening angle of hood will give A, C, B And D with respect to the ground. those A, B, C & D are decided in the head zone. Opening angle varies from region to region depending on average human weight. Depending on the standards we are deciding the angle. So, from the angle data, Support rod or Gas stay is designed. The position of Support rod is on the other side of the battery.
2.Adding latches and stiffener pad: Latches are added where and all the weight is added. On the inner panel we have Hinges and striker, which are attached to the inner panel so due to this attachment the strength of the inner panel is going weak. In order to strengthen the inner panel Latches will play a very important role. Stiffener pad is the sponge-like material place b/w Inner and outer panel to reduce vibrations.
3. Mastic Seals: Mastic Seals place b/w Inner and outer panel to reduce Noise, vibration, and harshness. Every Mastic will have an effect of 80mm Dia locally. Inner and outer panel gap is 1.7mm to 5mm.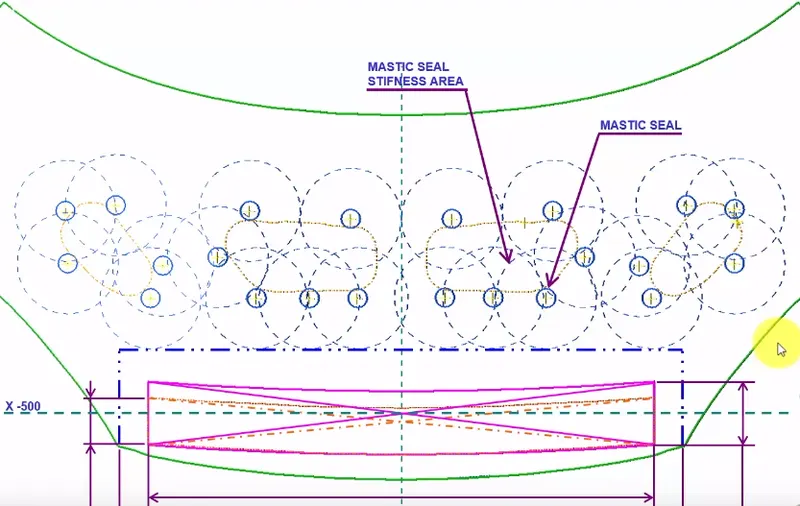
4.Emboss definition: Emboss are provided in the inner panel of the hood assembly. This helps in weight reduction of the hood and also to dissipate the force during collision.
Deep drawing is a sheet metal forming process in which a sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions. A flat sheet metal blank is formed into a hollow body open on one side or a hollow body is formed into a hollow body with a smaller cross-section.
Embossing
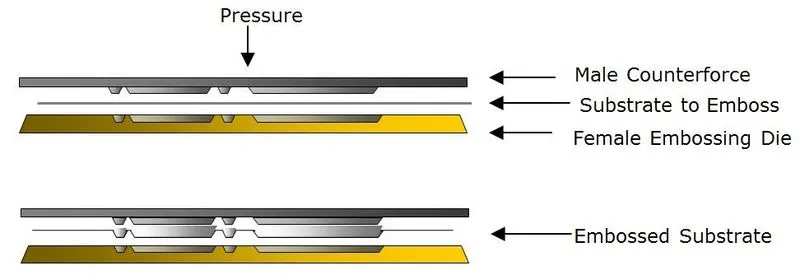
Embossing is a sheet metal forming operation related to deep drawing. Embossing is typically used to indent the metal with a design or writing. This manufacturing process has been compared to coining. Unlike coining, embossing uses matching male and female die and the impression will affect both sides of the sheet metal.
Hemming
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas or material roll-in. This is why it is important to use simulation tools in order to, on the one hand, better understand the hemming process and, on the other hand, significantly reduce the number of “trial and error” loops during try-out und production.
There are various types of hemming operations:
- Conventional die hemming
- Roll hemming
In conventional die hemming, the flange is folded over the entire length with a hemming tool.
In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
Hood for Better Pedistain Rating:
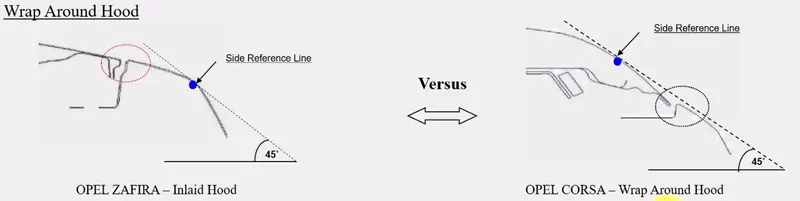
Inlaid Hood: The line which is drawn 45 deg. from ground to Side Reference of car and which is meeting point on fender is called Inlaid Hood.
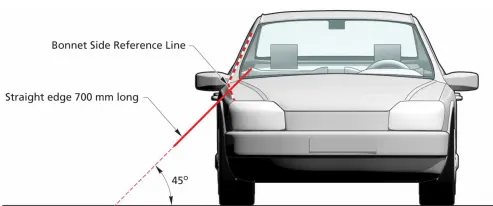
Wrap Around Hood: The line which is drawn 45 deg. from ground to front surface of the Hood and which is the meeting point on the outer panel is called Inlaid Hood.
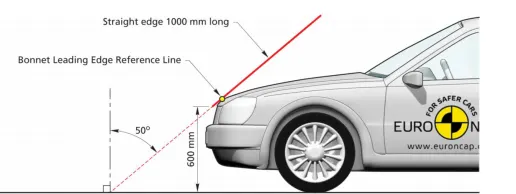
Depending on the Inlaid Hood & Wrap Around Hood we can design hood for head impact in the shown position of head impactor.
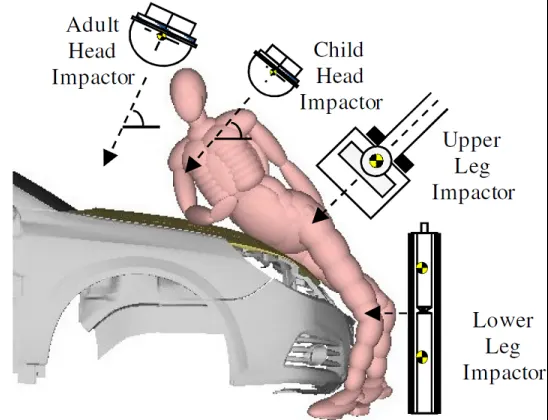
Position of head Impactor
So based on the position of head impactor we are providing emboss and cuts shown in the below figure.
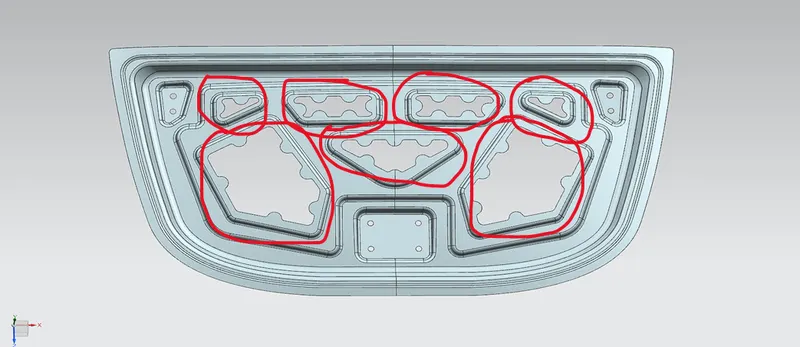
Design Procedure
- Import the file: File > open > browse file and select the given file
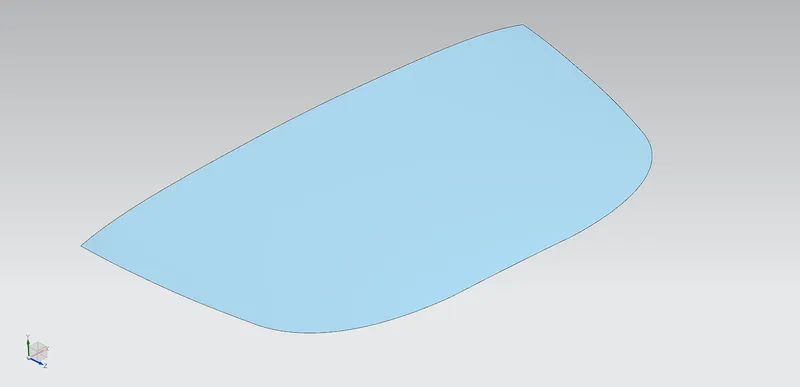
Inner Panel Design:
Given surface is A class and we have Design Inner outer panel using given class A with the help of the Given master section shown below figure.
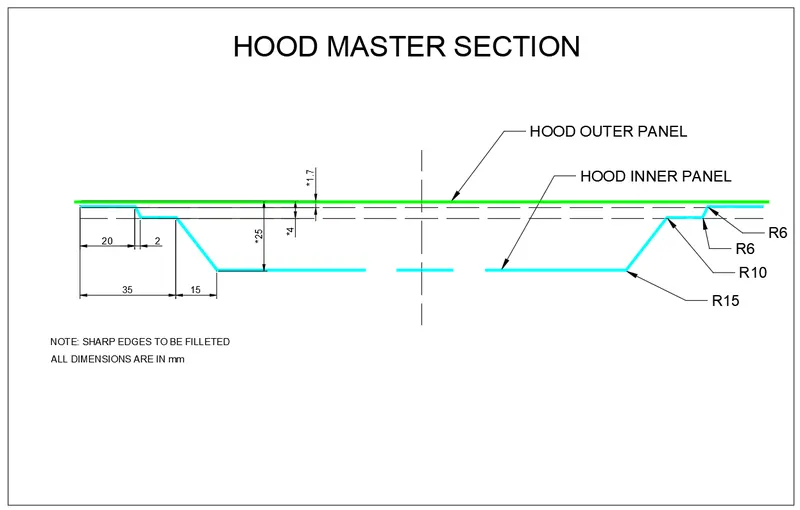
From the master section
- From the given surface offset to 1.7mm and split the surface with symmetry axis.
After dividing through symmetry axis create the tooling axis using perpendicular line as below.
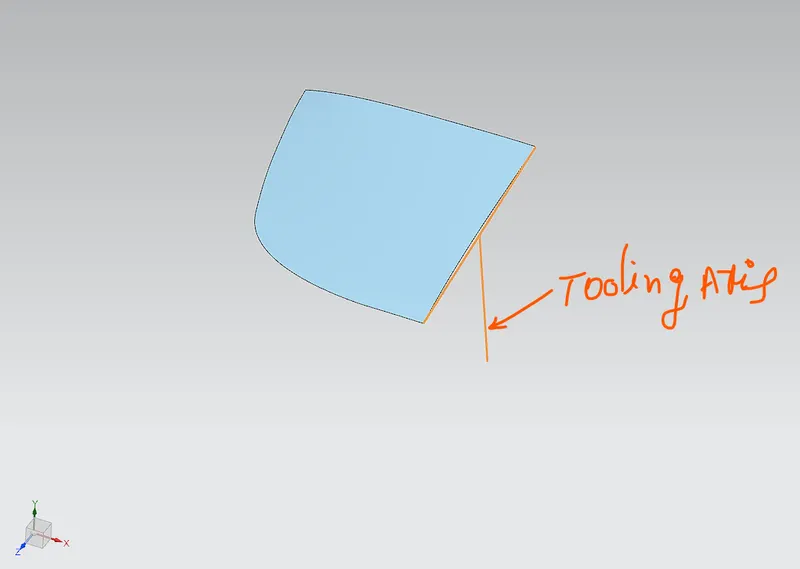
2.Create a boundary around the given surface and use offset in face tool to make boundary to 20mm from the master section. Trim the surface using the offset line shown in the figures to create first flange.
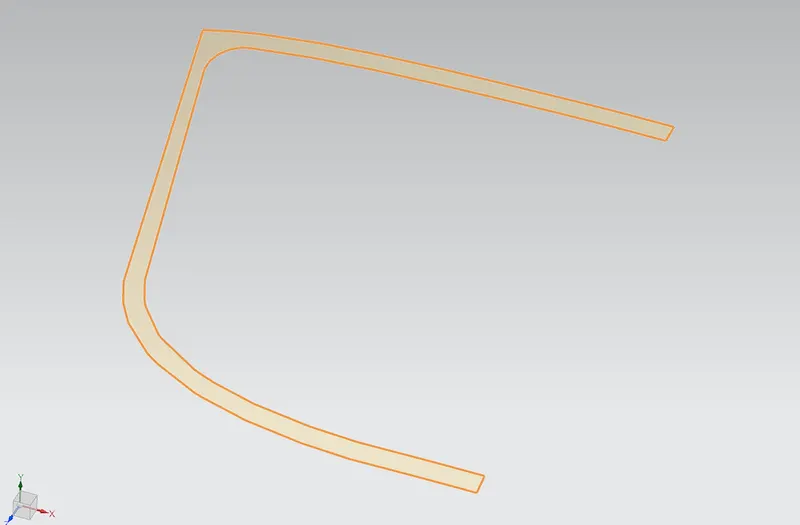
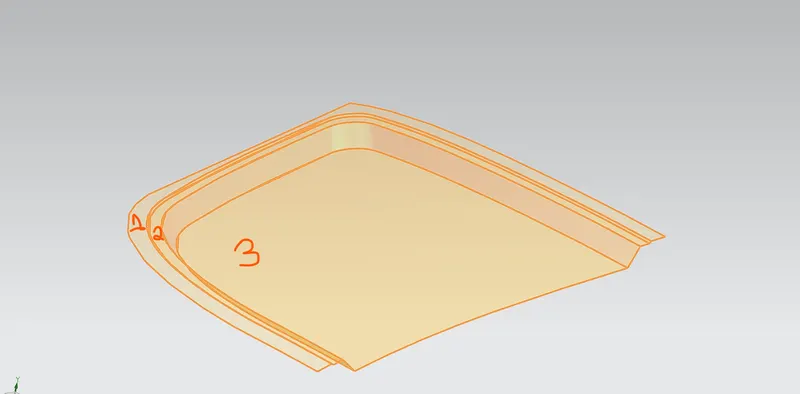
All 3flanges created with same procedure and connected through curves command the figure as follows:
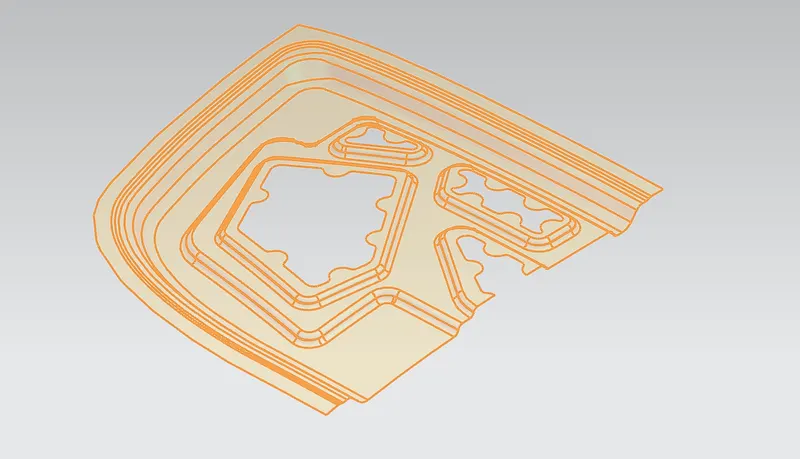
After creation of 3 flanges emboss and cutting operations done to reduce weight of the hood and safety of pedestrian. The final product is visible as follows:
After the above operation hinge emboss created which is parallel to ground and opposite to the cutting emboss. The image looks like below.
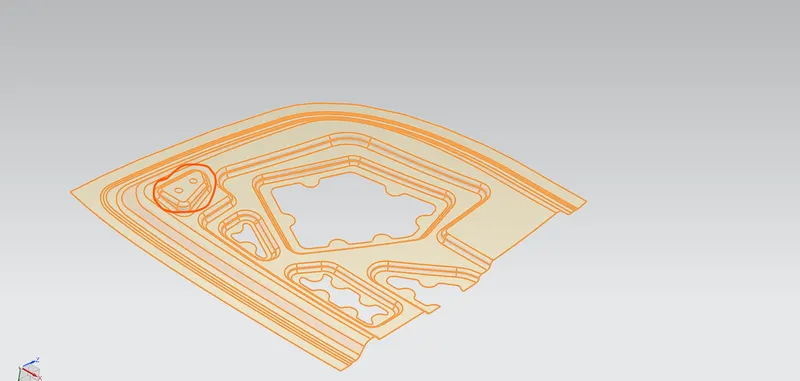
After creation of hinge mount, we create the axis of hinge and latch section which will help to create latch mounting emboss and position of latch mounting emboss.
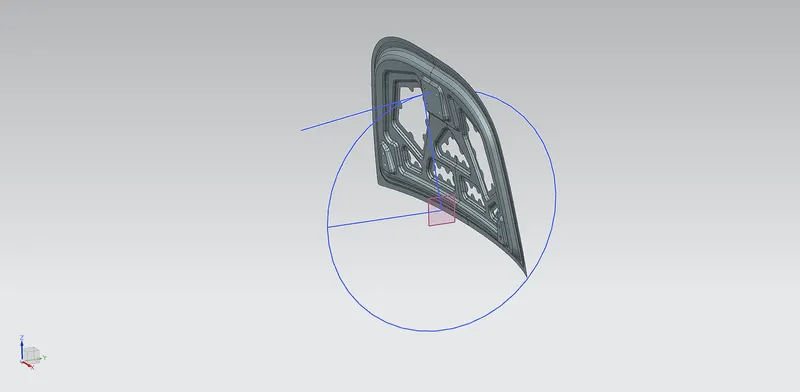
After above process will thicken the surface as per requirement of 0.75mm which is mentioned in the master section.
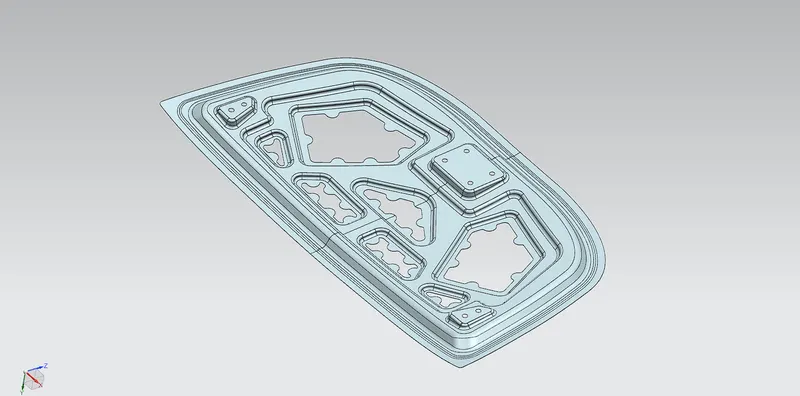
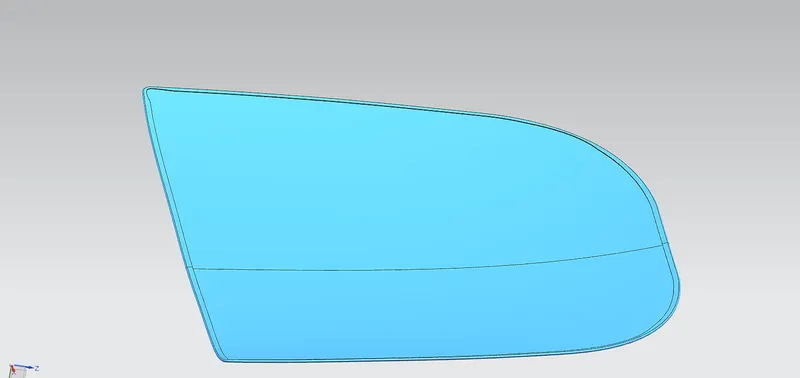
With the same procedure Hood outer panel is also created with hemming and corner hemming reliefs, provided thickness of 0.75mm and the image looks below
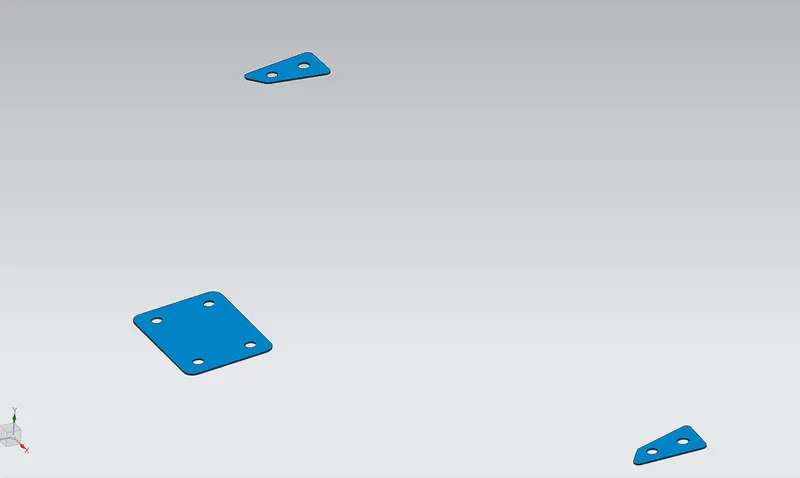
The reinforcements also created for making the hood strengthen at hinge fitting and latch& striker portions. The components are looks like the below
The final assembly as follows:
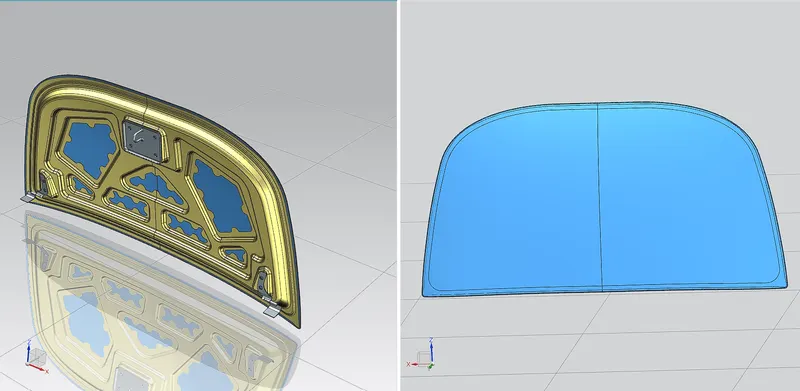
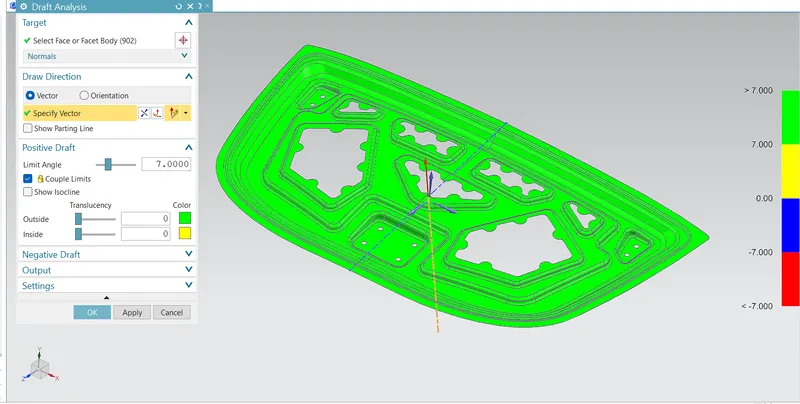
Draft Analysis:Draft analysis is a method of checking the draft angle on various faces of a part with a particular direction. it should be more than 7 deg.
In the following figure show the draft analysis for the inner panel.
Conclusion:
As per the given conditions the hood assembly is created.