Design of backdoor
DESIGN OF BACKDOOR
Aim: Designing the Backdoor by Using the provided styling surface to come up with a back door design and using appropriate design methodologies and make the necessary reinforcements and embosses.
What is a back door?
A door is a hinged part which is used for entry and exit of the vehicles. Back doors are one of the type doors of the vehicle which are located next to the passenger seat which provides access to the luggage compartment. In most of the cars, these back doors are operated with the help of gas stay which in turn reduces the effort required to lift open the door. Some luxury cars have powered backdoor which in turn is driven by an electric motor. This kind of system is also called a powered trunk lid system. Hatchback or station wagons are sold as 3 door or 5 door models. In this case, the rear hatch is classified as door this is because it enters the passenger compartment. The naming is mainly used in Europe countries. In case of safety, the back door designed should meet the safety requirement for the rear collision.
Types of the back door based on working positions.
1) Top-mounted:
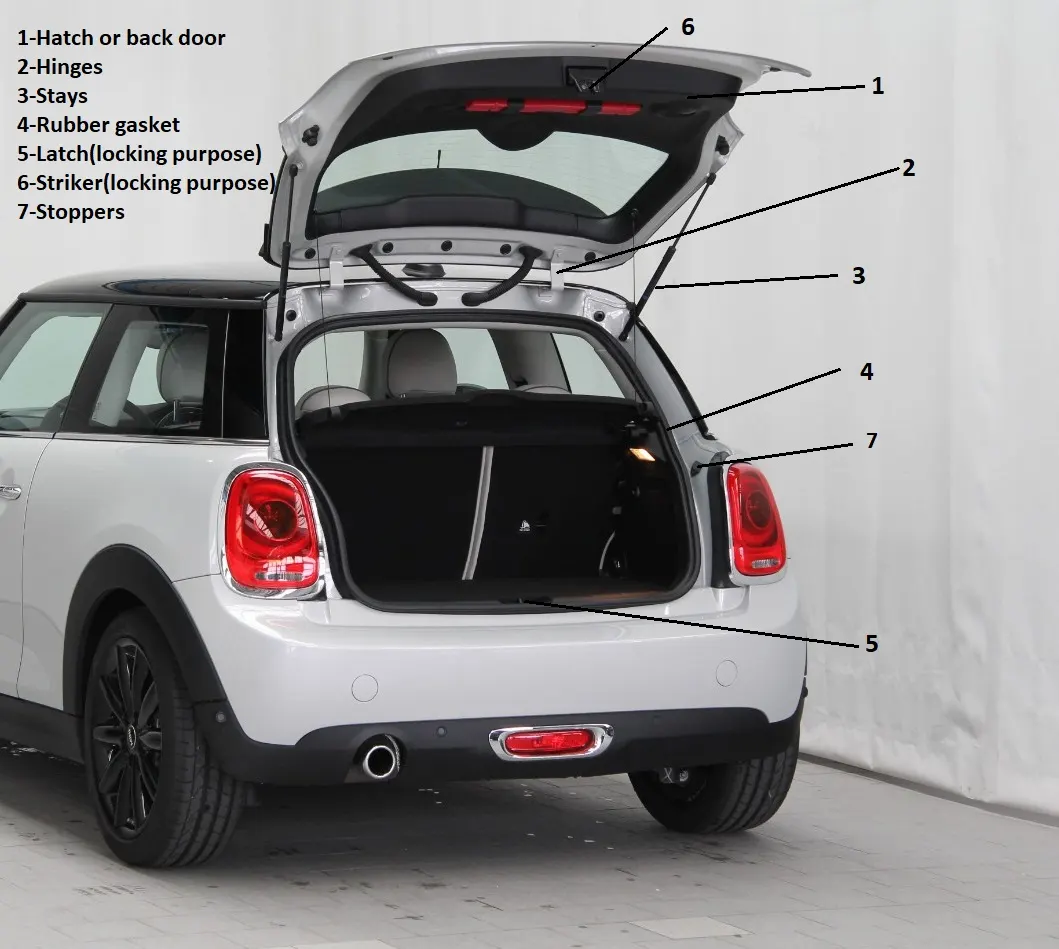
This type of back doors is used in a station wagon, pickup truck and some of the sport utility vehicles. Today’s modern cars use top-mounted tailgating systems which are both powered and also gas stay supported. These top mounted tailgates provide greater rear visibility compared to side-mounted or bar doors which have canter pillars in it.
2) SIDE MOUNTED DOORS:
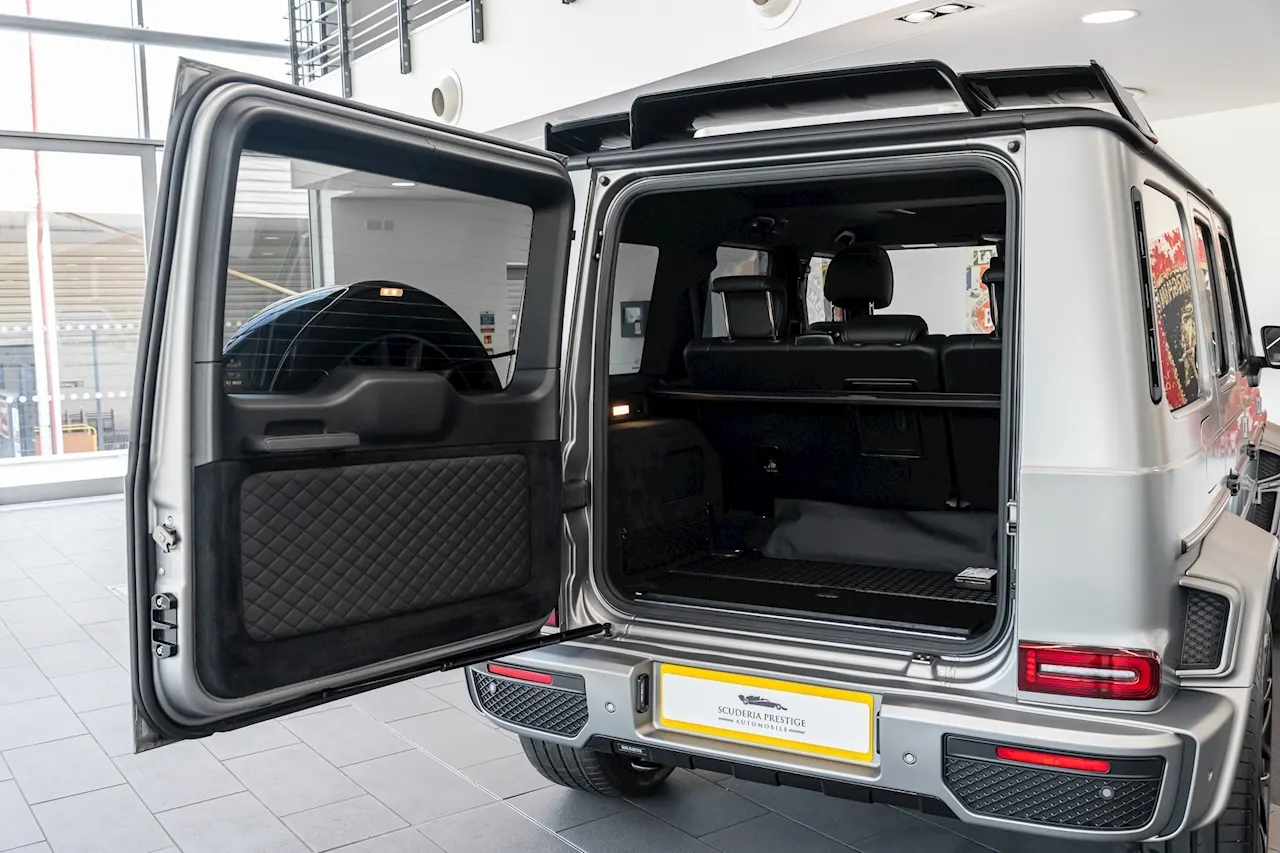
As the name signifies side-mounted doors are the one which is used in the van type MPVs, SUVs, pickup truck vehicles. These side-mounted doors or barn doors are a lot easier compared to top-mounted doors. These doors are generally smaller in size and can be easily accessed. These doors are more convenient for the goods handlers for long pipe and lengthy components where one door is kept open. These doors also save accidental head impacts. It is a lot easier to load and unload items in the side-mounted doors.
3) Bottom / Split type:
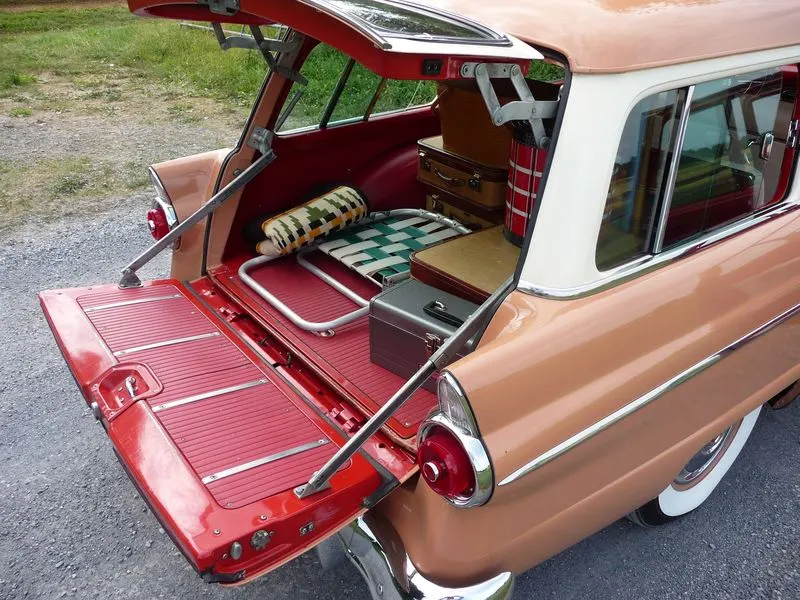
This bottom type or split type backdoor system are used in the car type such as estate type car, pickup trucks and some luxury SUVs. These are the most convenient type of back door in which the bottom split is used as a support or even as a table for the tour going people.
Types based on working mechanism.
1) Gas stays type:
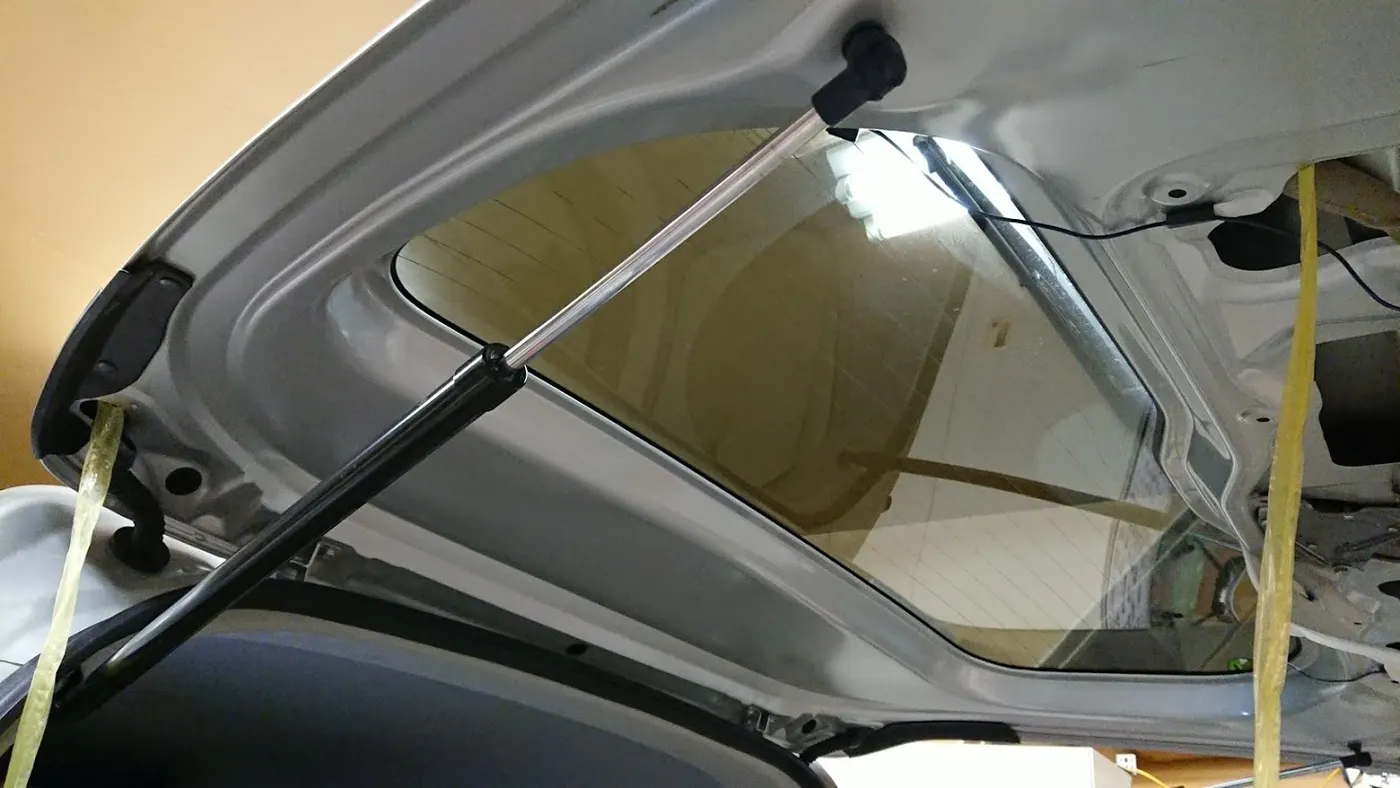
Gas stay types backdoor/liftgate/tailgate is an ideal and most commonly used tailgate mechanism from lower segment car to luxury car segment. The ideal components of tailgate consist of a hinge, door, gas stay and some rubber beadings for sealing of door which is shown in the image below:
Power Spindle system:
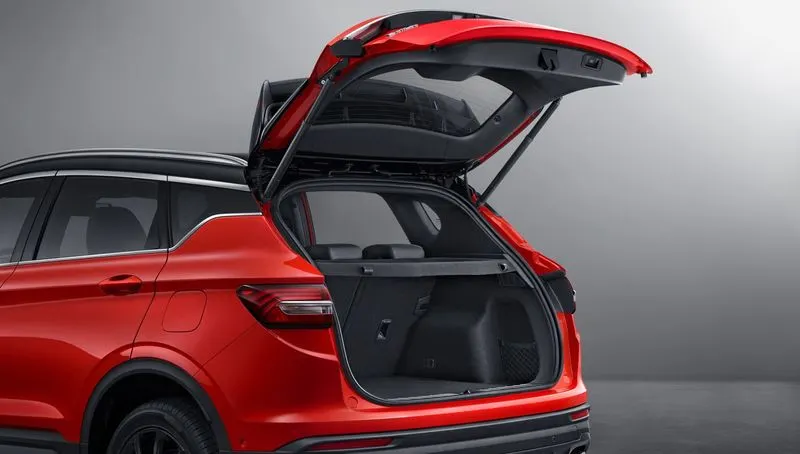
Power trunk lid system is another sophisticated way of trunk/liftgate opening mechanism which is to automatically open and close of the trunk/liftgate and release of the latch by the touch of a button. The following image shows the component as used in the powered trunk/back door lift system.Powered trunk lift system consists of a power latch, anti-pinch switch, PTG ass’y, PTG main switch. When the switch is pressed in the compartment or outside the power latch releases the latch and the entire backdoor is opened. The anti-pinch switch is located in order to avoid accidental hand insertion during the operation of the door.
Back door Lock-
The locking of the trunk may be achieved together with the passenger compartment.
Some cars include a function to remotely open the trunk. This may be achieved through a variety of means:
- release of the latch whereby the doorseals push the decklid away from the lock, the trunk is then open, and the lid may not have revealed the opening.
- release of the latch whereby a spring pushes the decklid away from the lock and open, the trunk is then open, and the lid reveals the opening.
- release of the latch and actuation of a drive, whether hydraulic (BMW 7 SERIES) or electric (BMW X6), which pushes the decklid away from the lock; the trunk is then open, and the lid reveals the opening. This may then be electrically closed again.
Images of Car Back door Lock (Latch)
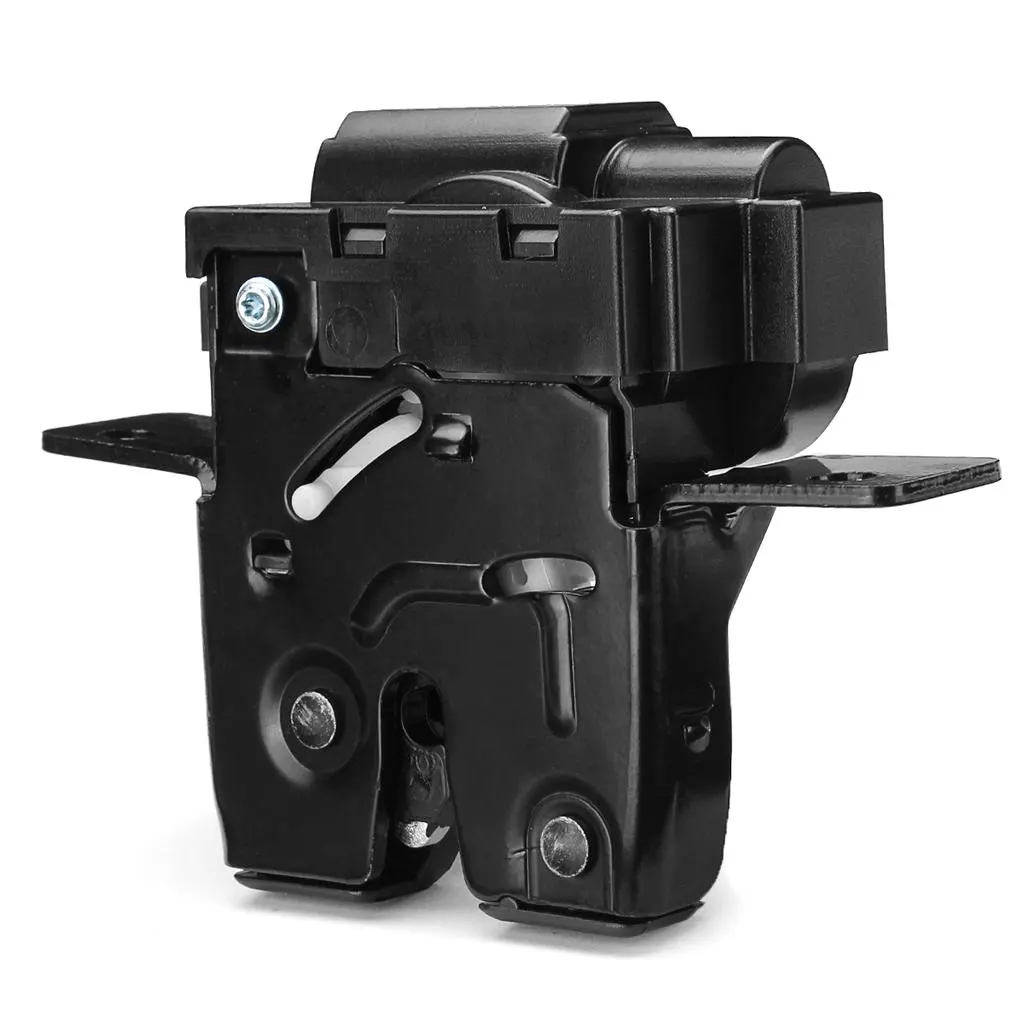
Latch arrests the striker to lock the backdoor of a Car
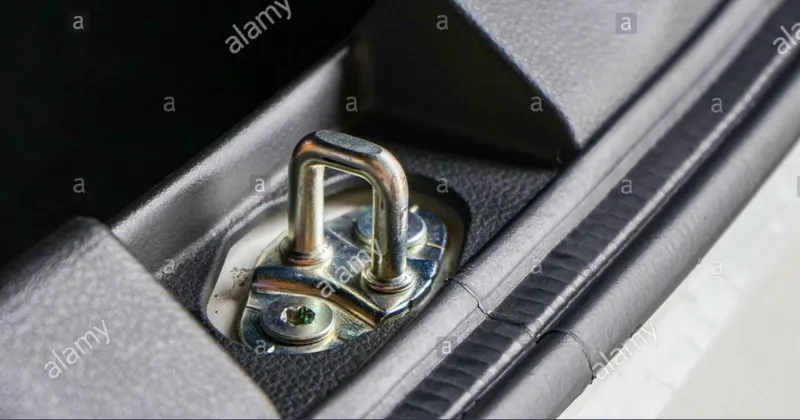
Image of a striker
Hinge-
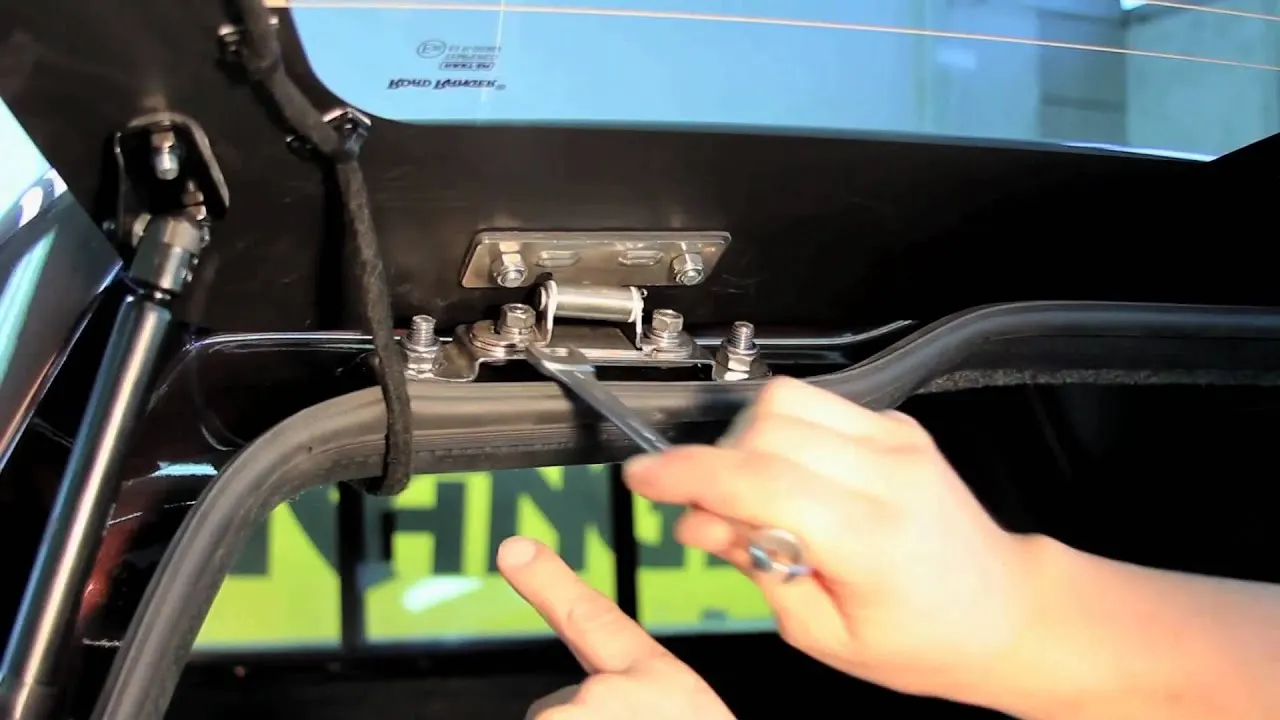
A hinge is a mechanical bearing that connects two solid objects, typically allowing only a limited angle of rotation between them. Two objects connected by an ideal hinge rotate relative to each other about a fixed angle of rotation: all other translation or rotation being prevented, and thus a hinge has one degree of freedom.
Image of a Back door Hinge
- Rear Wiper Motor-
Rear-window wipers are typically found on hatchbacks, stations wagon / estates, sports utility vehicles, minivans, and other vehicles with more vertically-oriented rear windows that tend to accumulate dust. So a motor is required to move the wipers.
Image of a wiper & motor
Materials Selection:
The selection of Material plays a major role in determining the overall weight of the back door. The common materials used are Steel & Aluminum. The density of Steel is higher than Aluminum thus adding more weight to the door. The material used in the manufacturing of the backdoor depends upon the budget of the car, most low cost vehicles use steel as it is cheaper compared to Aluminium. Another aspect to be noted is that, if casted Aluminum parts are used instead of deep drawn steel parts there is no need of reinforcements and the overall weight of the car is reduced by approximately 5-10kg thus increasing the performance of the vehicle. Also the draft angle for casted parts is around 3 degrees while for deep drawn parts is around 7-10 degrees which helps in increasing the luggage/ cabin space.
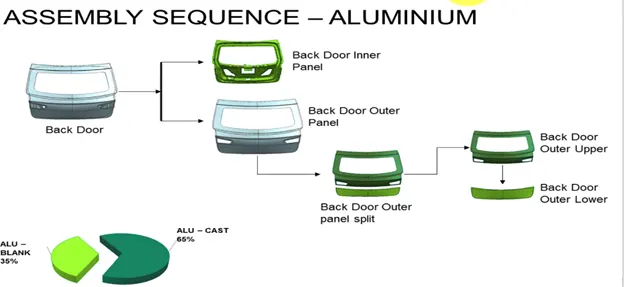
Fig. above shows possible no. of parts in aluminium backdoor
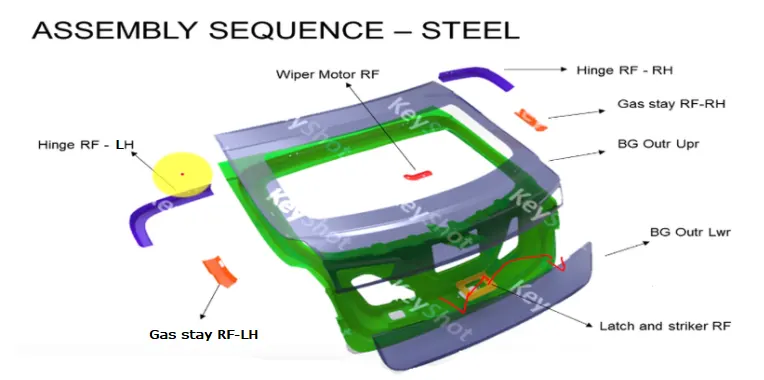
Fig. above shows possible no. of parts in Steel backdoor
The below table gives a comparative information about Steel and Aluminium.
| Aluminium | Steel | |
| Parts | Parts are casted | Parts are stamped |
| Reinforcements | Reinforcements can be neglected | Reinforcements are necessary |
| Thickness | Thickness can be varied | Thickness should be uniform |
| Weight | Lighter in weight | heavier in weight |
| Cost | Costly as compared to Steel | Cheap as compared to Aluminium |
| No. Of components | Less No. of components | More No. of components |
MANUFACTURING METHODS:
Recently, there have been two approaches to reducing automobile weight. One is by using material lighter than steel and the other is by redesigning the steel structure. Although the former seems very effective, it is very expensive so that it may only be used for an expensive automobile. Therefore, the automobile industry is trying to use steel, which is not costly and recyclable. Lightweight steel can be achieved by improving the performance of the structure or adopting new manufacturing techniques. One of the efforts is the ULSAB (ultra-light steel auto body) concept.
ULSAB suggests three main weight reduction techniques such as hydro-forming and the tailor welded blank (TWB).
Tailor welded blank:
A tailor-welded blank is a blank that is comprised of two separate pieces of sheet metal that have been welded together prior to stamping. Tailor welded blanks allow the welding of the different grades, different thickness or different corrosion coatings together in order to give the properties needed in different areas, without increasing the number of tools needed to form the part and eliminating the fit ability concerns. They also allow a high degree of flexibility in designing parts and large blanks can be formed from much smaller sheets. The use of tailor-welded blanks would reduce the weight of the car. Having the ability to selectively place different thickness of material would result in weight reductions. An example of this used in production is the door inner panel. The only strength requirement on a door inner is in the region where the hinges attach to the panel.
Different Sheetmetal processes used for manufacturing the Back Door
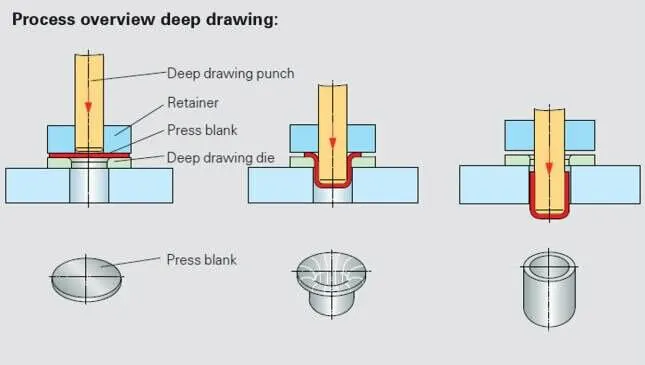
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
- First- stage drawing: The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
- Redrawing: The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing.
Embossing:
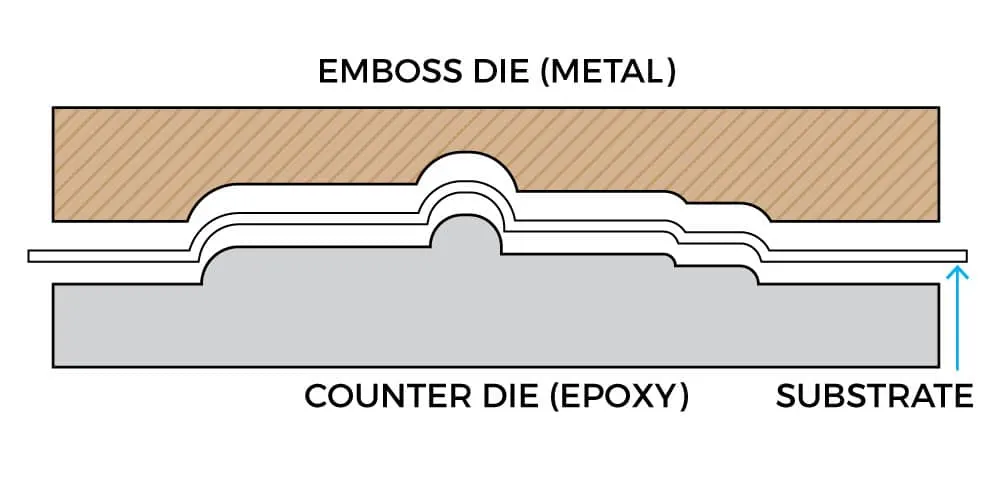
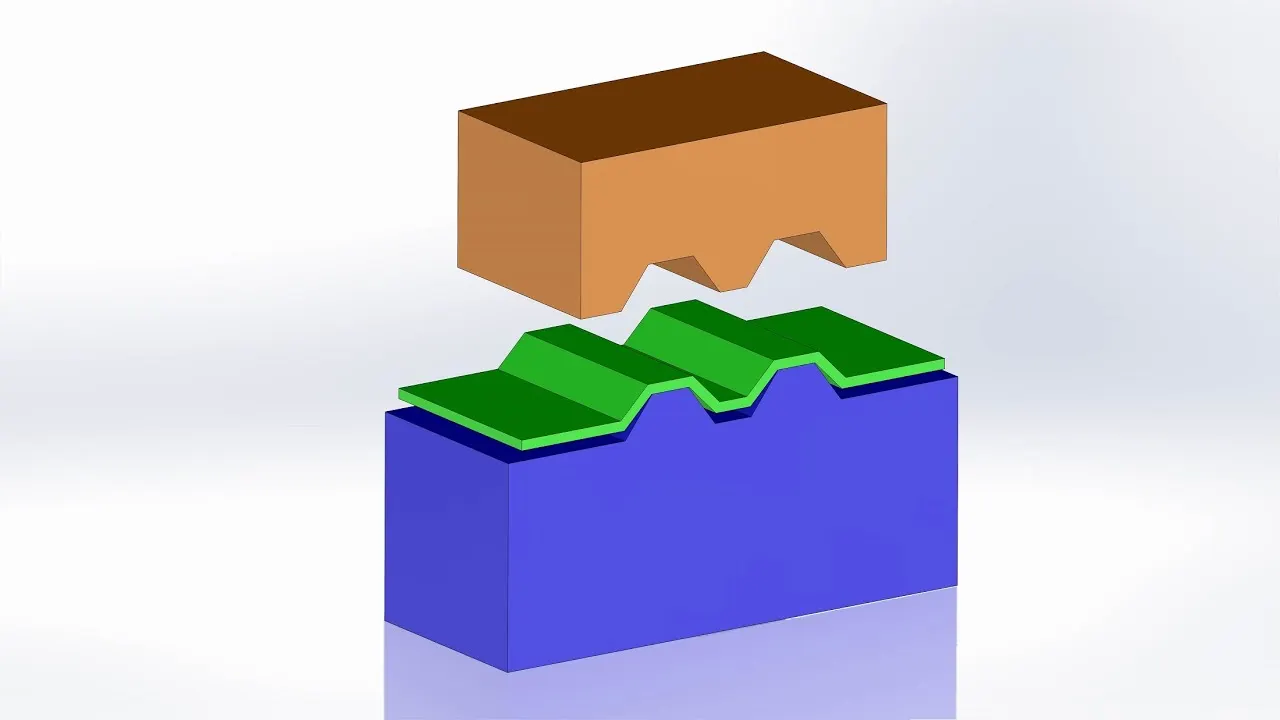
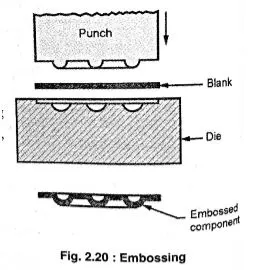
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
Lancing-
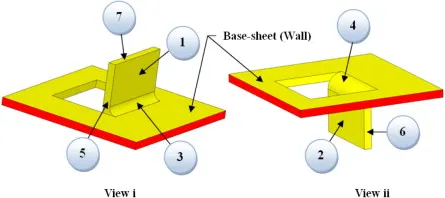
Lancing is a piercing operation in which the work piece is sheared and bent with one strike of the die. A key part of this process is that there is not reduction of material, only a modification in its geometry. This operation is used to make tabs, vents etc.
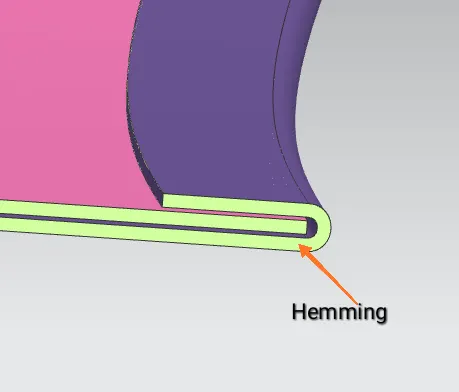
Hemming:
Hemming is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
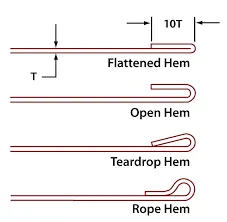
There are various types of hemming operations:
- Conventional die hemming: In conventional die hemming, the flange is folded over the entire length with a hemming tool.
- Roll hemming: In roll hemming, the hemming roller is guided by an industrial robot to form the flange.
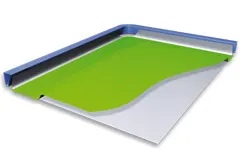
Open Hem: A Hem has a full round feature and a return flange. In open hem bend angle is equal to 180 degrees.
Tear drop Hem: In tear drop hem the bend angle is greater than 180 degrees.
Closed Hem: Hems without any inside radius are called as closed hem. Closed hems are not recommended if the hem geometry is to be painted or if the material used is SST or Aluminium.
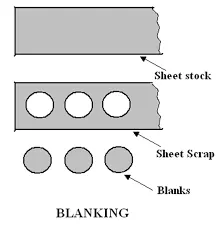
Blanking:
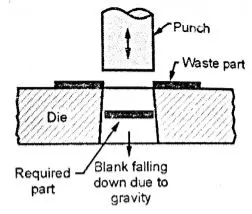
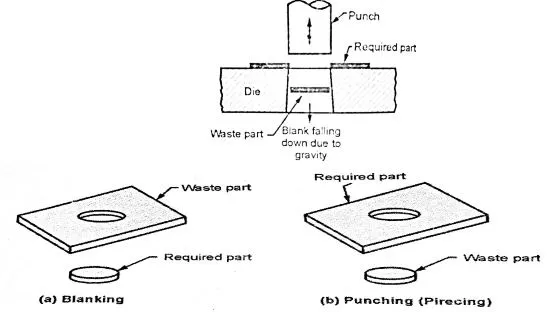
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered as a waste.
Punching:
It is similar to blanking only the main difference is that, the hole is the required product and the material punched out from the hole is considered as a waste.
Mastic Sealant-
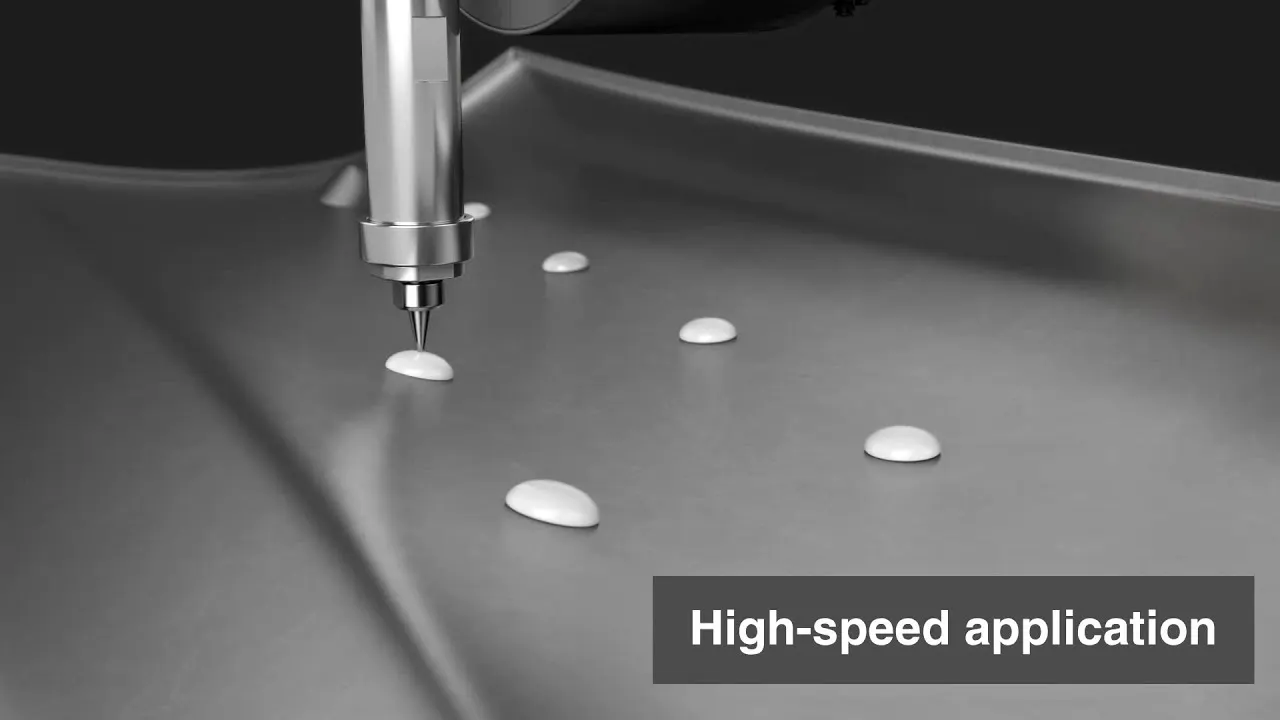
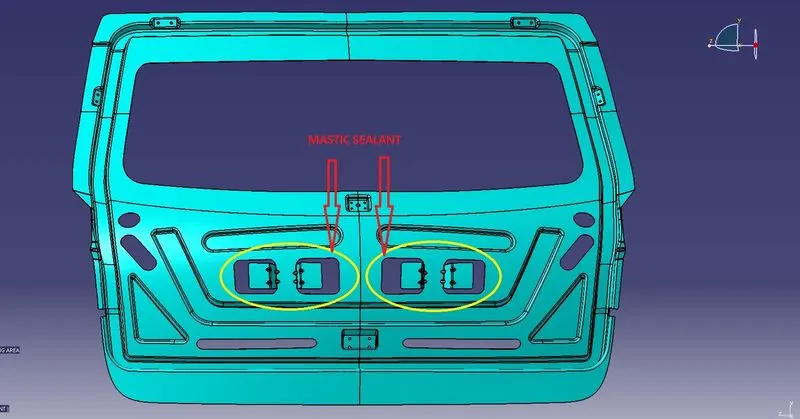
A mastic sealant is a type of liquid sealant that cures in an elastic state, thus making it flexible while holding the bond of the surfaces that has attached together. It adheres to just about any material making an all-purpose type of sealant.
- The main purpose of the outer panel is for the aesthetic looks. Thus we cannot use bolts or welding. This has to be done with the help of the hemming and mastic sealants. Mastic sealants are elastic compound that behaves like the rubber. It is placed between the outer and inner panel. Initially is it in paste form, but after the hot furnace bath it gets hardened thus joining the outer and inner panel. Mastic sealant has the tendency to increase the strength of the panel and has influence of 80mm diameter.
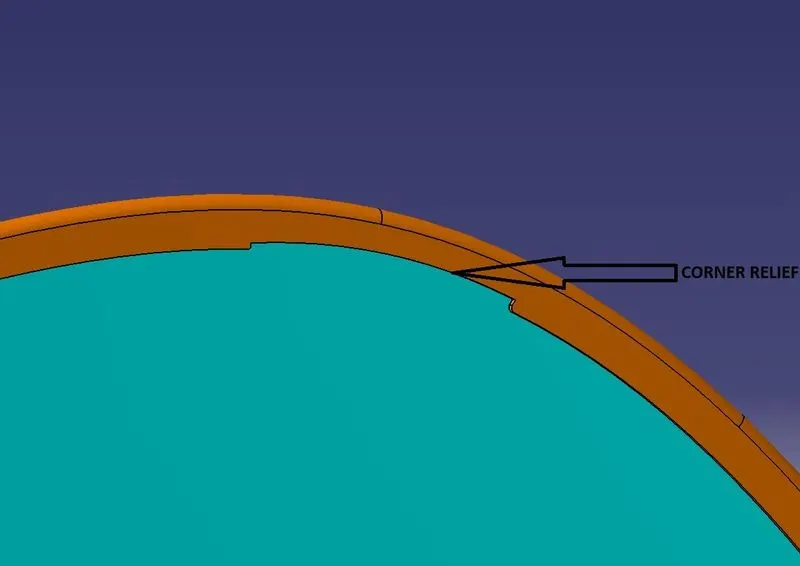
- Corner Relief-
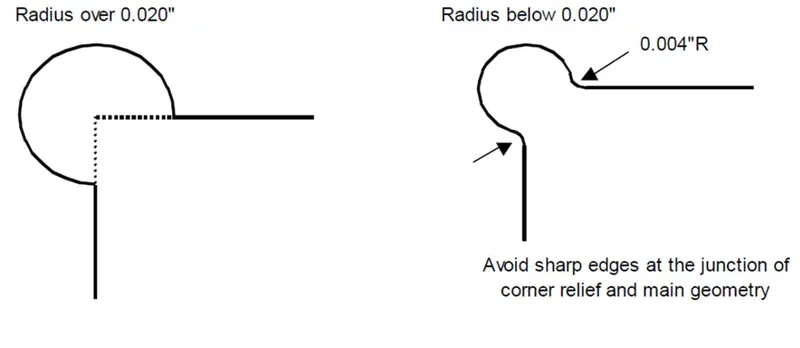
Relief is provided onto the part or component in order to remove any stresses developed in a particular area i.e sharp corners that takes place during the hemming process is carried out. Thus corners are rounded or chamfered.
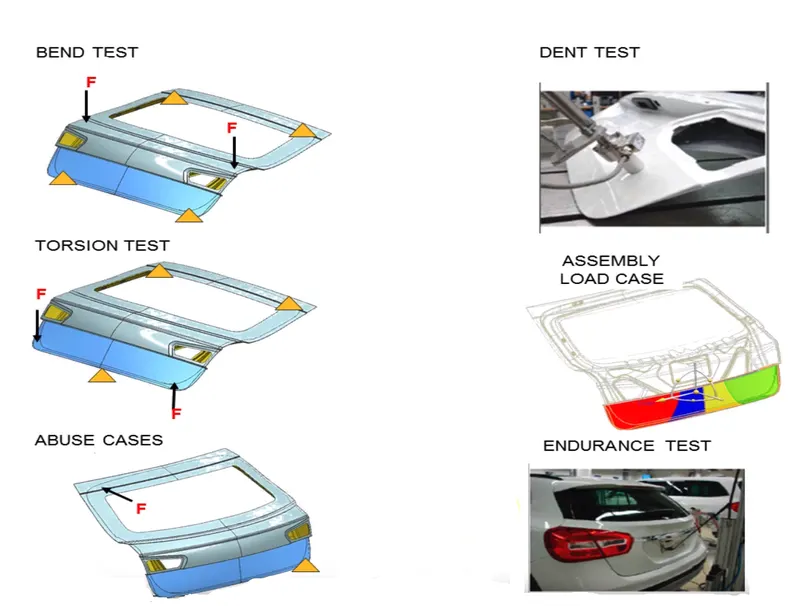
Some Tests that are performed on the Back door to check the strength, quality and durability.
BACK DOOR ASSEMBLY:
The back door assembly of a hatchback or SUVs has the following components.
- Inner panel
- Outter panel upper
- Outter panel lower
- Hinge reinforcement LH
- Hinge reinforcement RH
- Gas stay reinforcement LH
- Gas stay reinforcement RH
- Wiper motor reinforcement
- Latch reinforcement
- Plastic trim
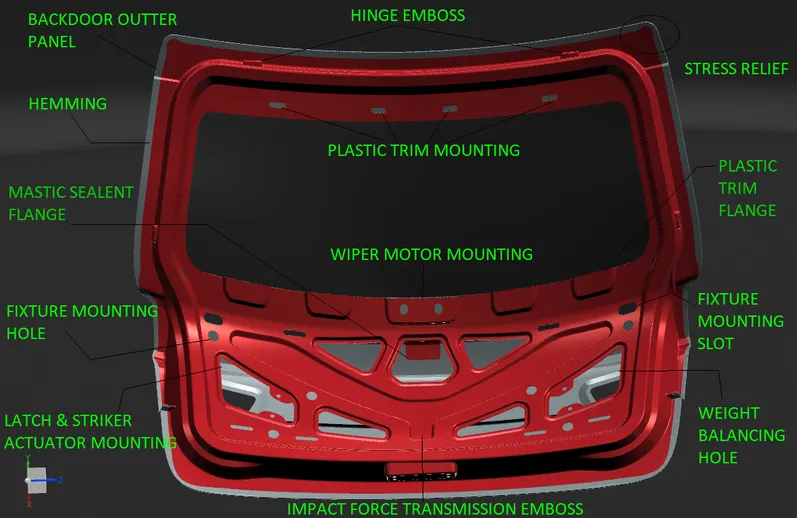
Above image is for Reference purpose only
DESIGN INTENT
The intent of the project is to design a Body In White Back Door of the vehicle considering the engineering standards and manufacturing requirements which satisfies the Deep Drawing Process.
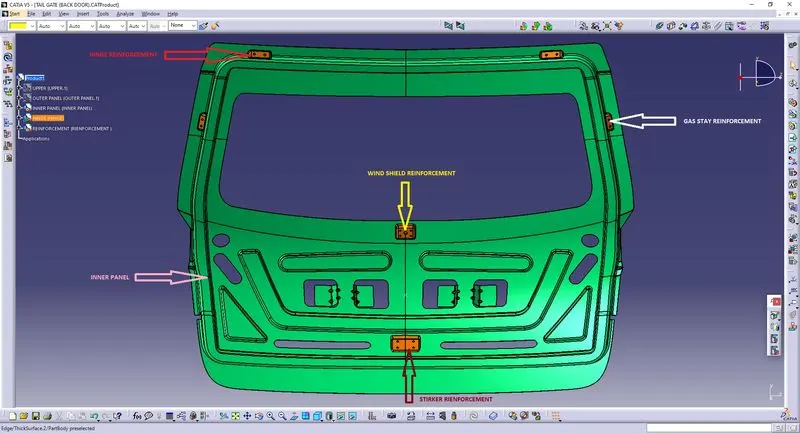
DESIGN CONSIDERATION OF A BACKDOOR:
-
Functional Requirement of Hinge and gas stay
-
Rear visibility criteria
-
Luggage volume
-
Crash Analysis
-
Bend Test, Dent Test, Torsion Test & Endurance Test
-
Rear Crash Regulation
-
Gap and flushness Requirements
DESIGN OF BACKDOOR OUTER PANEL:
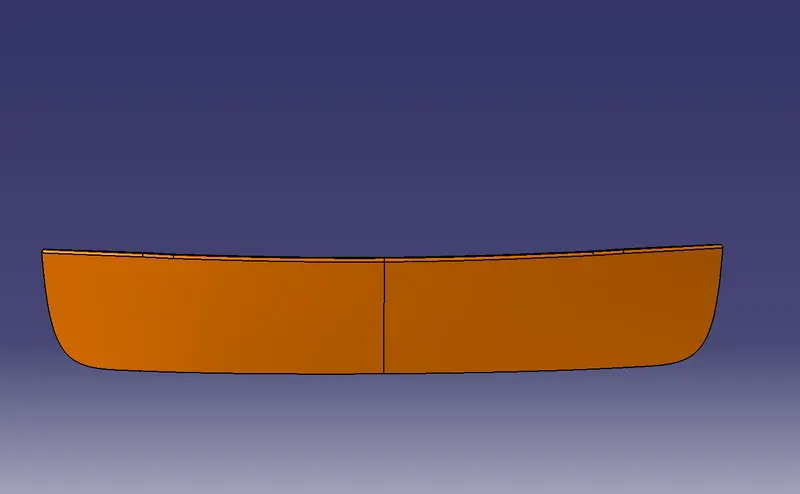
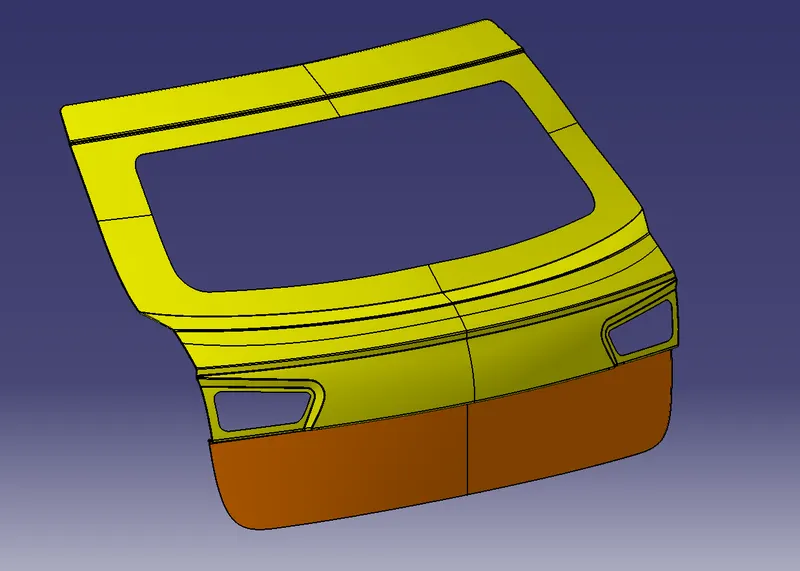
The Outer Panel is the styling surface of the back door. Other components of the backdoor are designed with reference to the outer panel. It acts as the outer cover and deals with the aesthetics of the car.
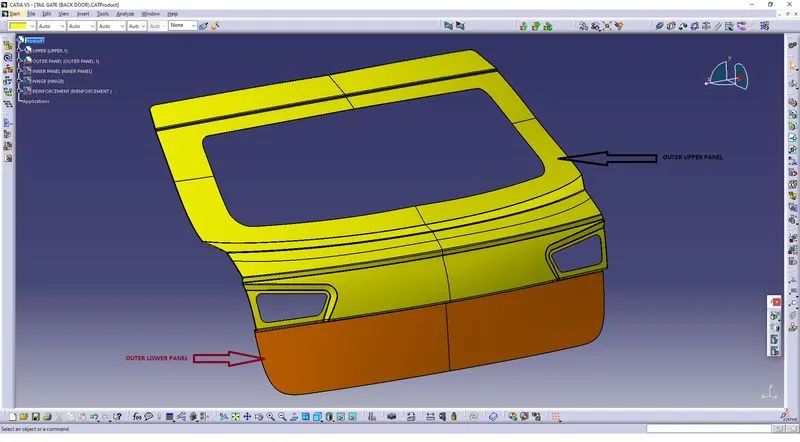
In this design outer panel is divided into two parts
-
Outer Upper Panel
-
Outer Lower Panel
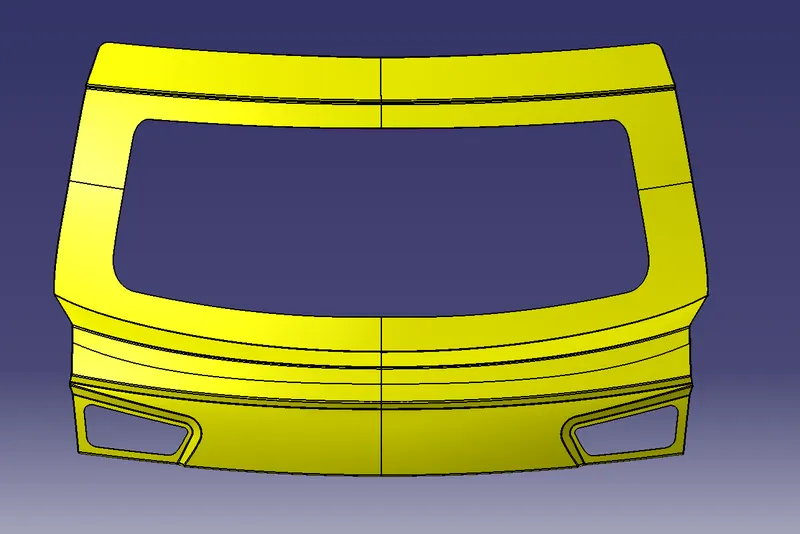
Outer Upper Panel:
- The Outer Upper Panel Extracted from a styling surface.
- The panel is altered for the required design with the surface tools CATIA V5.
- The thickness provided for the outer panel is 0.75 mm
- Hemming is provided with the corner relief.
Outer Lower Panel:
- The Outer Upper Panel Extracted from a styling surface.
- The panel is altered for the required design with the surface tools of CATIA V5.
- The thickness provided for the outer panel is 0.75 mm.
- Hemming is provided with the corner relief.
Outer Upper & Lower Panel:
Tooling Direction:
-
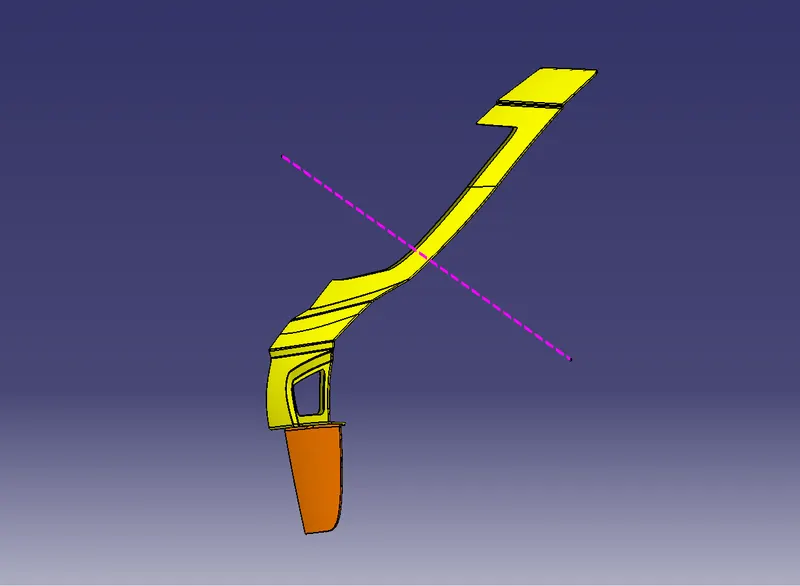
Before starting to design the inner panel of the back door the tooling direction for Deep Drawing purpose should be created.
-
Then the styling surface needs to be checked and analyzed since it might have irregularities, hence it must be fixed first.
-
Then the back door was designed using the top-down approach.
DESIGN OF BACKDOOR INNER PANEL:
- The Inner Panel Extracted from a styling surface.
- The panel is altered for the required design with the surface tools of CATIA V5.
- The thickness provided for the outer panel is 0.75 mm.
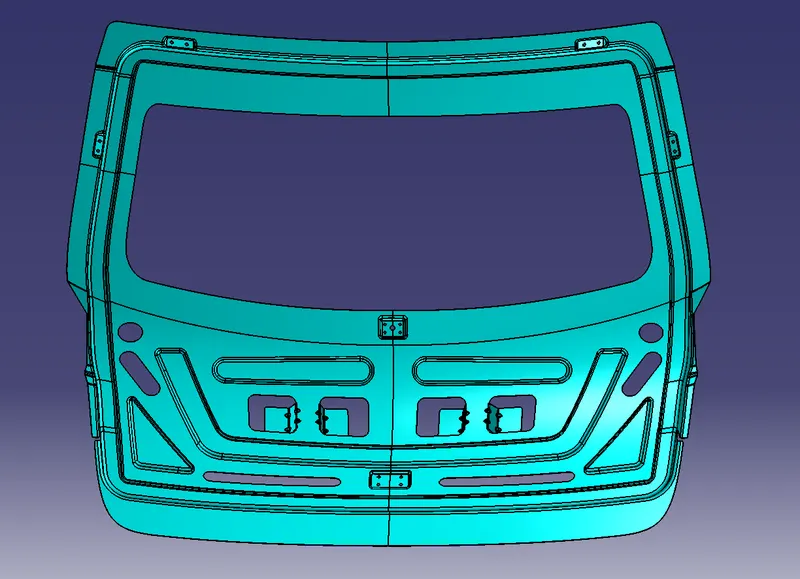
After creating the tooling direction the design of the inner panel will begin where we will first develop an effective sealing flange by checking all the boundaries and by following the shape of the inner panel design. By creating multiple flanges and by using surface modeling techniques the concept design of the inner panel was created.
-
After the concept of the inner panel is developed, then the child components like a hinge, latch, gas-stay locations, and their reinforcements must be designed. Which completes the overall design of the tailgate.
-
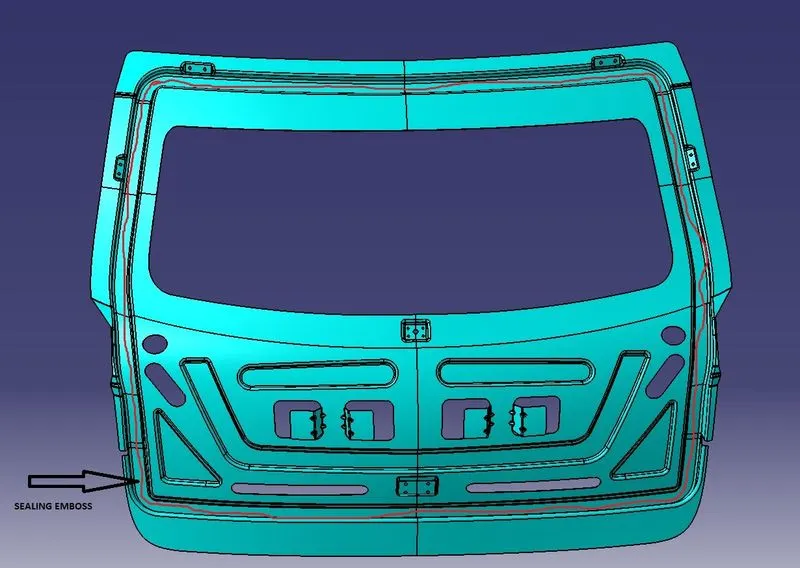
The embosses were created in ‘V-Shape or Y-Shape’ so that if the vehicle undergoes the crash then the force dissipates over it which reduces the damage transferred to the trunk space.
MASTIC SEALANT:
The mastic sealant is used to fix the inner panel with the outer panel which increases the NVH factor and stiffness of the back door.
HINGE, GAS STAY & WIPER MOTOR EMBOSS:
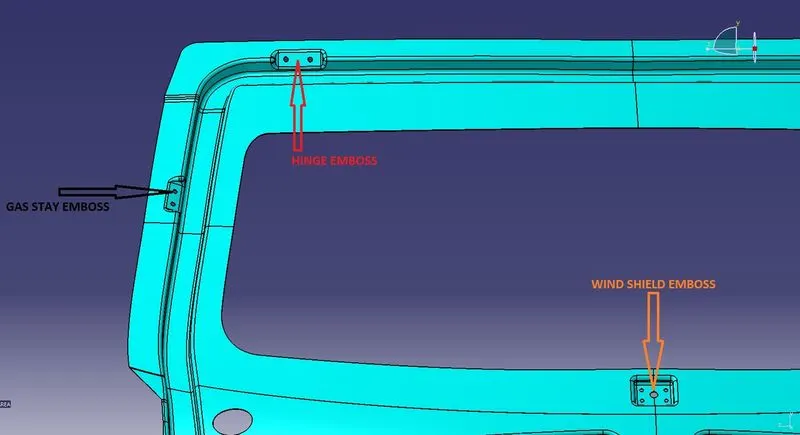
The Orange circle denotes the hinge emboss which was created using the datum plane and emboss feature in NX. It was also designed in a way that the emboss should have a flat surface for assembling the hinges using it.
The violet circle denotes the gas stay emboss which was created using the surface of the connecting flange.
The yellow circle denotes the Wiper motor emboss which was created using the surface of the connecting flange.
LATCH AND STRIKER EMBOSS:
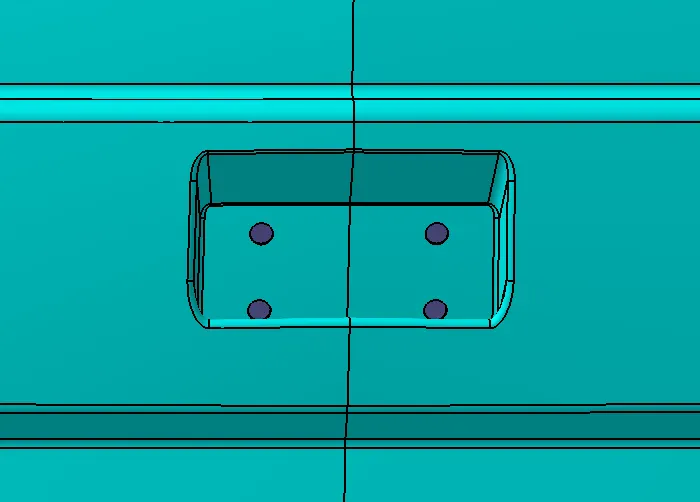
The Latch and Striker emboss were designed by creating a trajectory that follows the opening and closing of the back door with respect to the hinge axis.
HEMMING:
Hemming and seaming are two similar metalworking processes in which a sheet metal edge is rolled over onto itself. Hemming is the process in which the edge is rolled flush to itself.
-
The outer panel was designed as two separate parts named as outer panel upper and outer panel lower.
-
After designing the outer panel the Hemming was created by offsetting the surface with the help of face blend and swept surface.
-
The two separate outer panels will be joined using Blanking
CORNER RELIEF:
During the hemming process, when giving the Corner Relief helps to control sheet metal material behavior and to prevent unwanted deformation during unbend operations and also helps to reduce the number of passes in hemming.
DESIGNING THE REINFORCEMENTS:
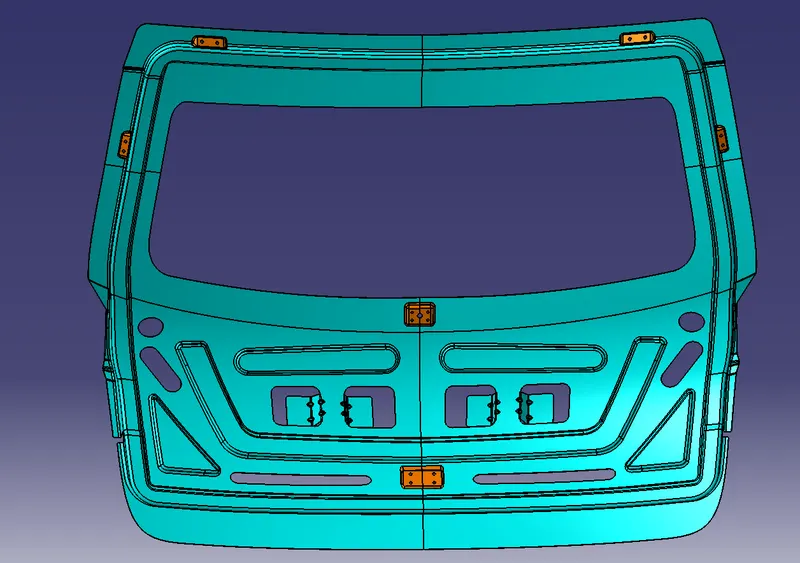
The thickness provided for all reinforcements is 1.5 mm.
-
HINGE REINFORCEMENT
-
GAS STAY REINFORCEMENT
-
WIPER MOTOR REINFORCEMENT
-
LATCH REINFORCEMENT
All the reinforcements were created using the same method, first, the linked body was created separately for each with the help of extract geometry and then the required portion was trimmed out and then thickened.
Hinge reinforcement:
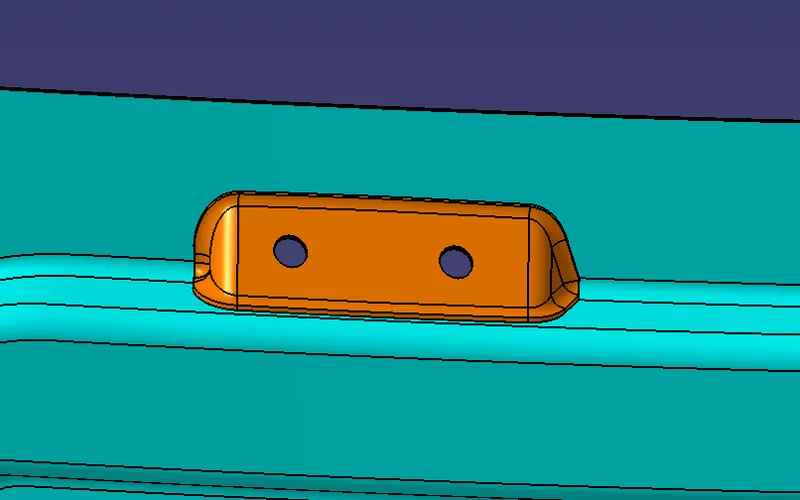
Hinges enable the opening and closing of the back door. One end of the hinge is fixed on the backdoor and the other end on the Roof, on both sides. Hinges can be placed outside or inside the backdoor.
The hinge reinforcements are added to compensate for the weak region due to the acting load over it.
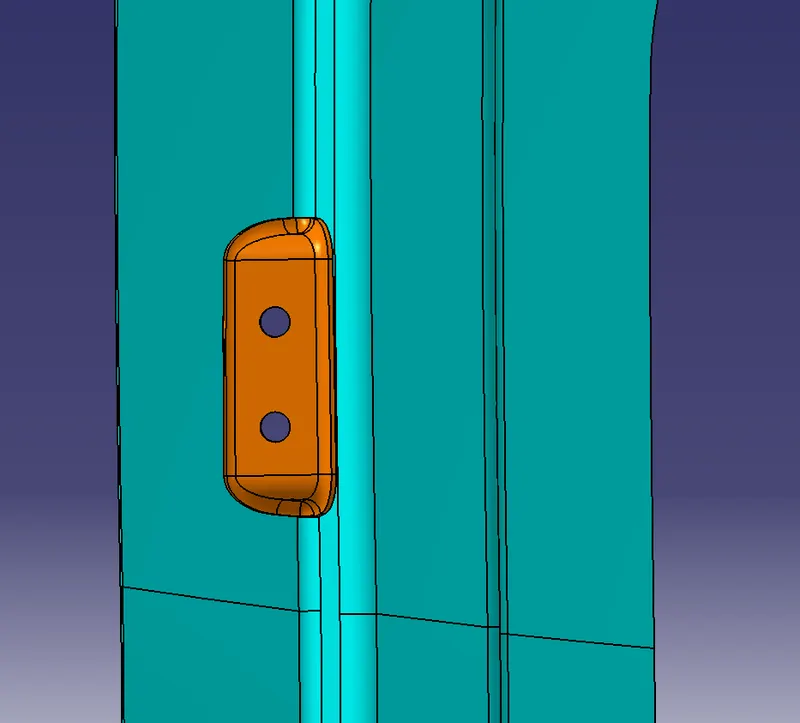
Gas Stay Reinforcement:
Gas Stay is a device used for supporting the back door in its open position. Gas stay requires no manpower and is engaged into support position automatically as the back door opens. One end of the Gas Stay is fixed on the backdoor and the other end on the Body Side or on the Back door stationary area.
Embossing is provided at the Gas Stay mounting area to compensate for weakness and improve strength.
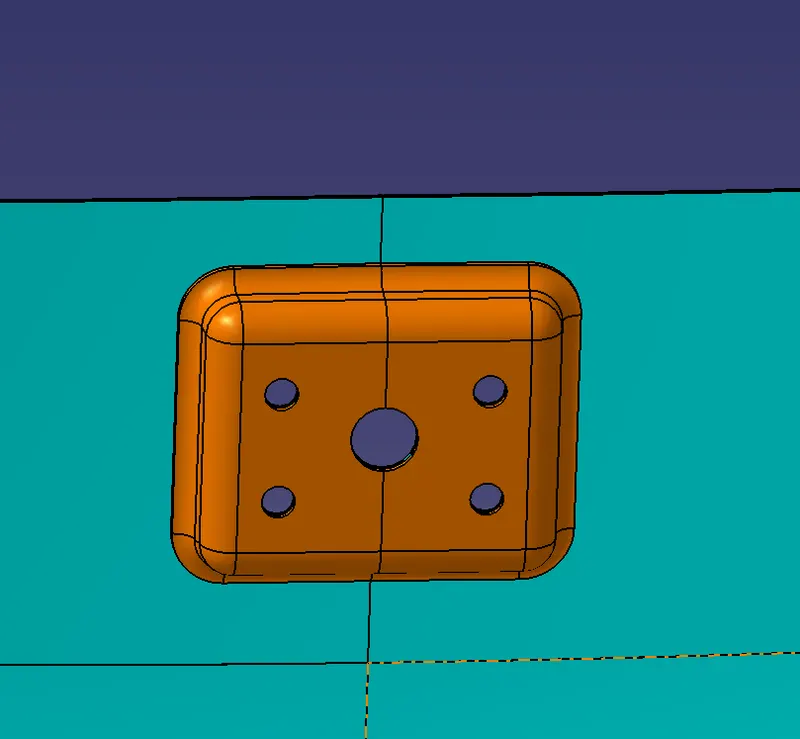
Wiper Motor Reinforcement:
Wiper motor reinforcement is created to mount the wiper motor assembly.
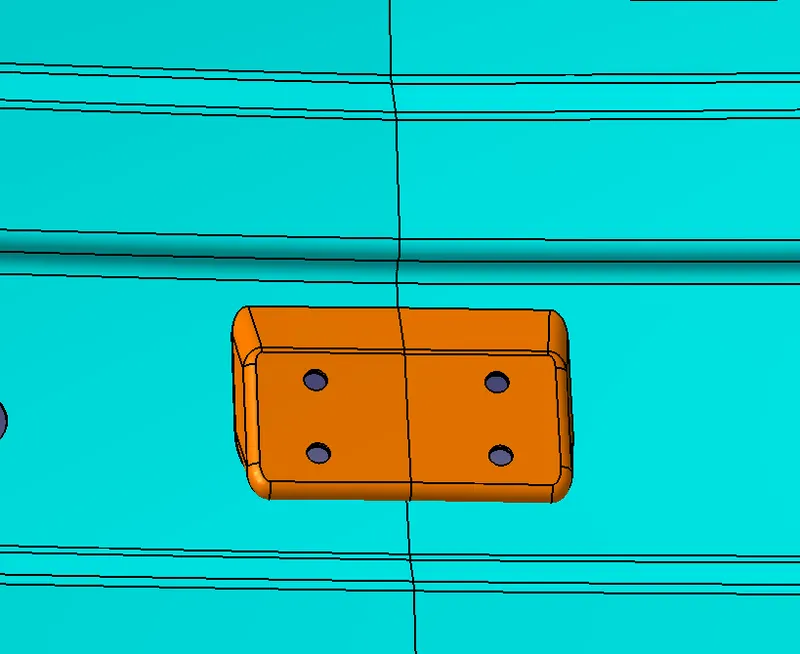
Latch and Striker Reinforcement:
The Latch & Striker forms the locking mechanism of the backdoor with the car. Due to regular opening, closing, and over slamming of the backdoor, there is stress developed in the Latch and Striker area. To compensate for the same, reinforcements are added in this area.
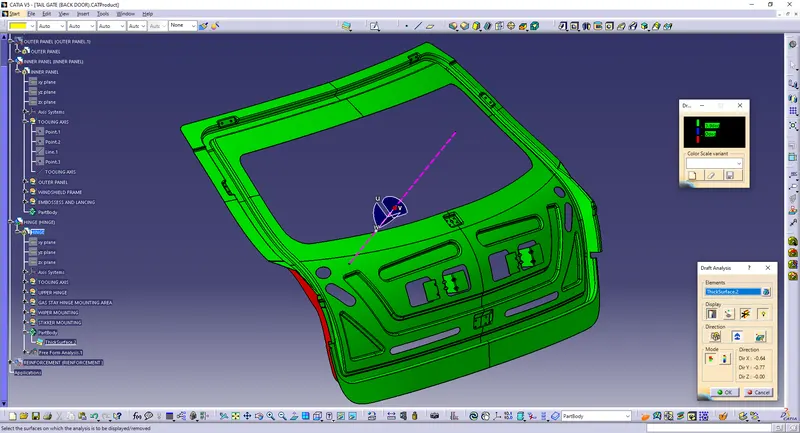
DRAFT ANALYSIS:
-
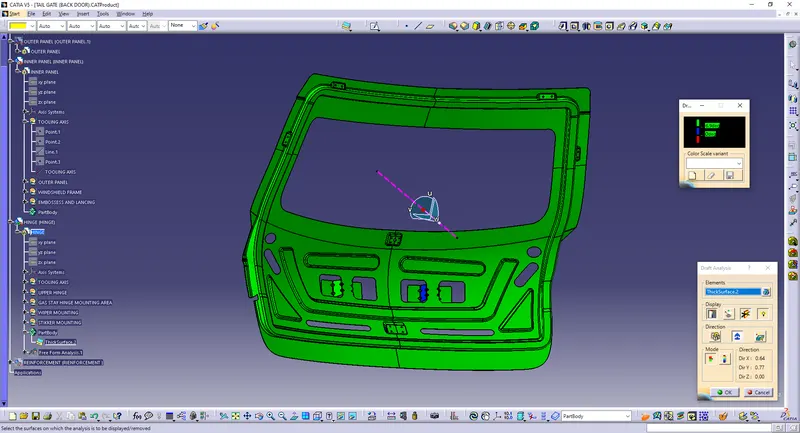
The draft analysis will be performed for the tooling direction created at first and checked that the model is suitable for manufacturing.
-
Then to get a complete green portion the necessary changes to the draft angle of the embosses were carried out by optimizing the model.
-
The Draft Analysis command enables us to detect that the part drafted will be easily removed or not.
-
This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
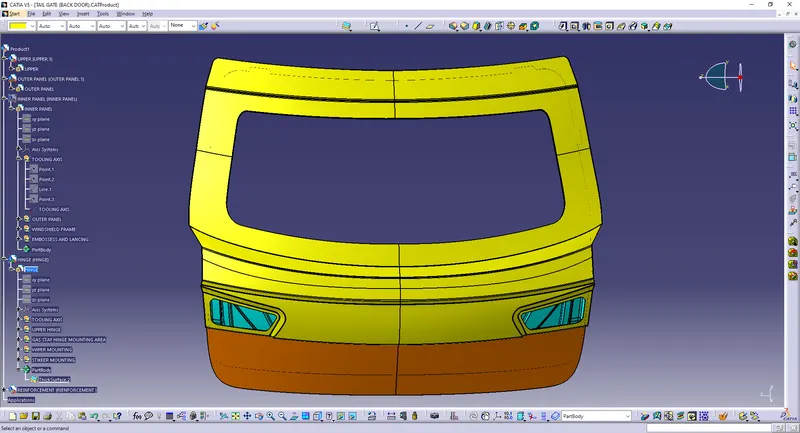
Views of the designed Back Door:
Front view:
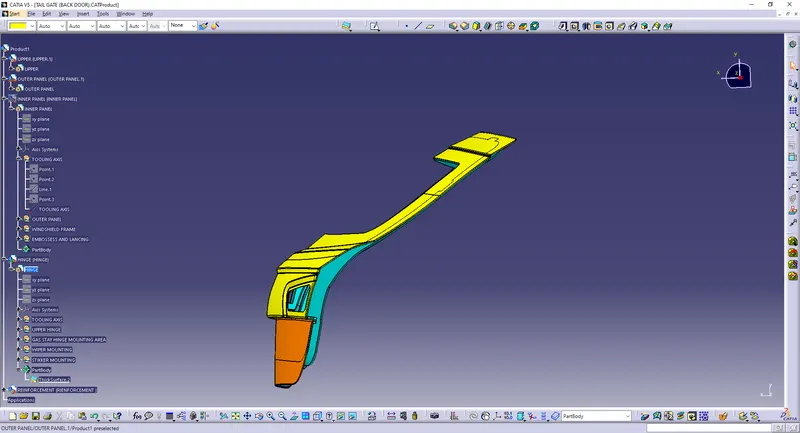
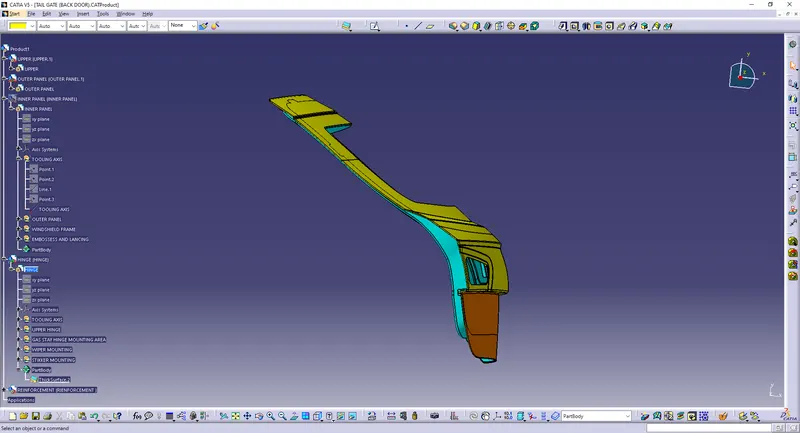
Side views:
Top view:
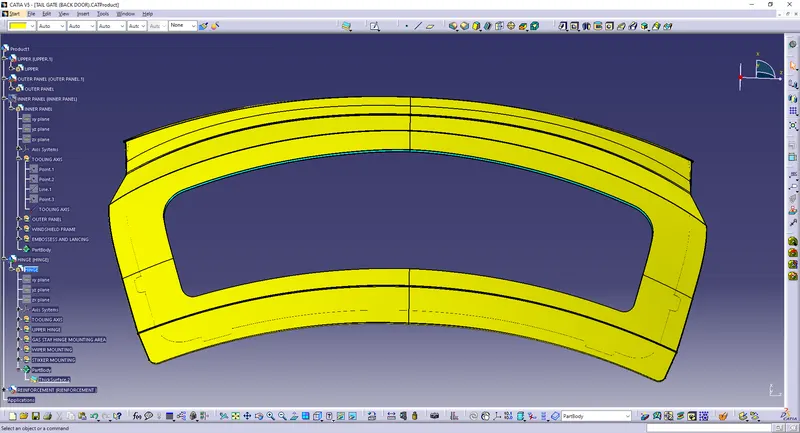
Bottom view:
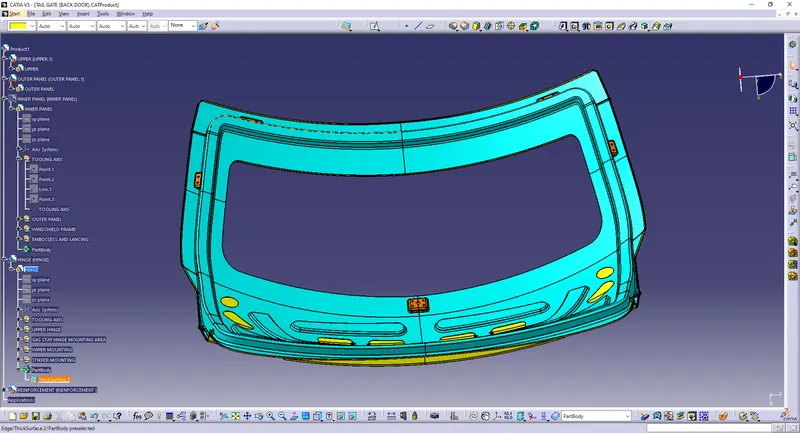
Back view:
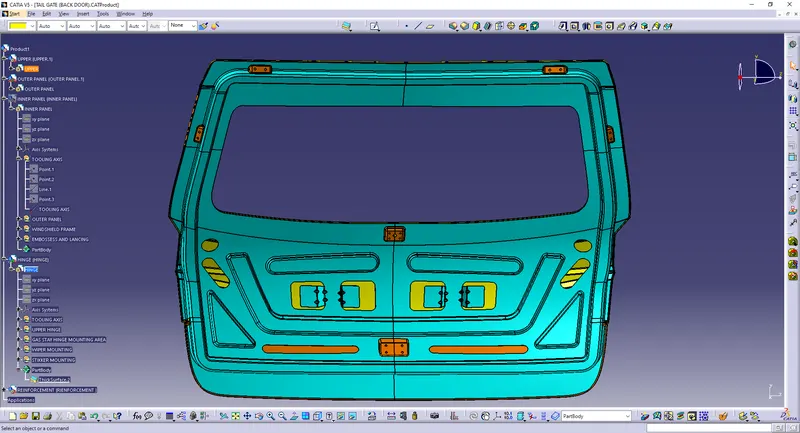
Isometric View:
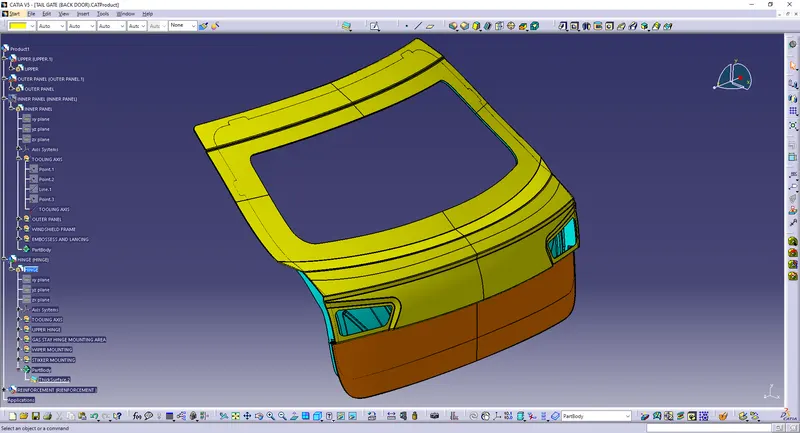
CONCLUSION:
Thus the Body In White Back Door of a car was designed following the engineering standards and also the deep drawing requirements were satisfied.