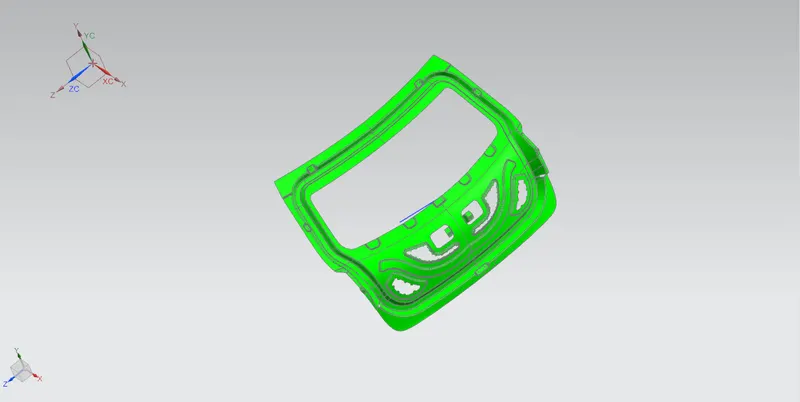
Design of backdoor
BACK DOOR ASSEMBLY
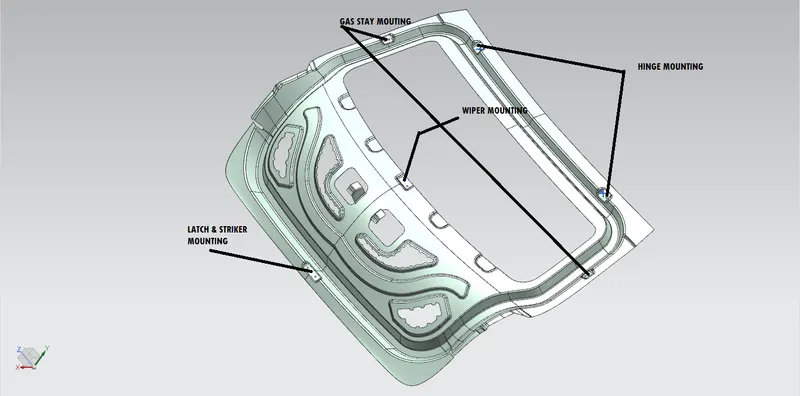
A back door is a BIW component found in all Automotive car generally used for opening and closing of the so called car luggage that is usually used for storing items inside a car. In general the opening and closing of the door is co-ordinated by the Latch and Stricker position and the Gas stay position that is mounted on the body and back door of the car. These positions play a major role in ensuring smooth opening and closing of the tail gate.
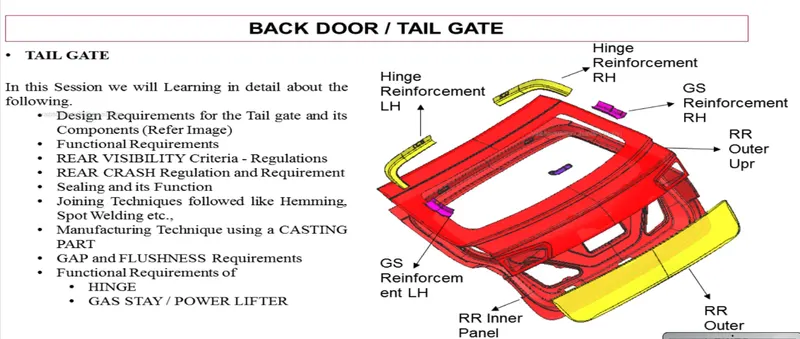
Parts of a Tail Gate:
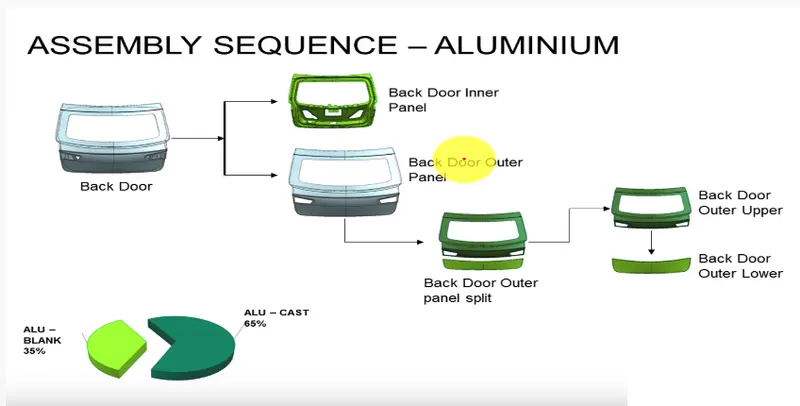
- Outer Panel
- Outer panel Lower
- Inner panel
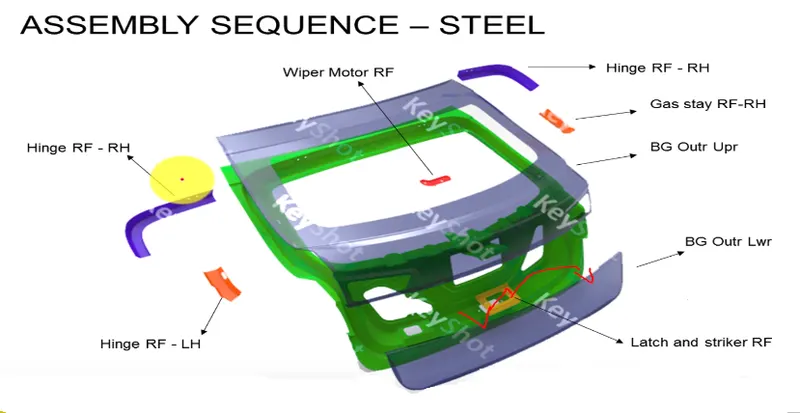
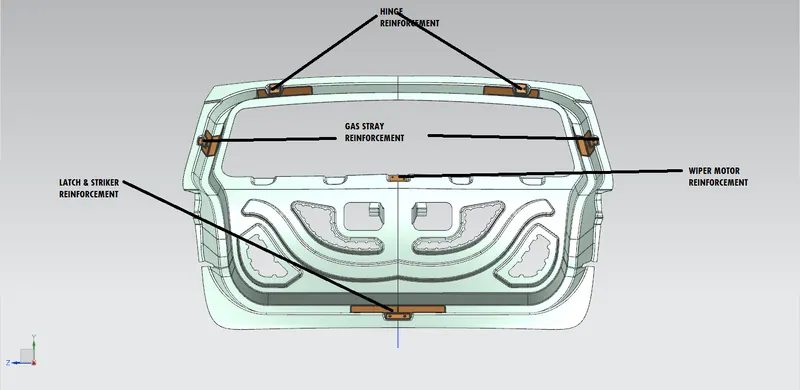
- Hinge Reinforcements
- Latch and Stricker Reinforcement
- Wiper Motor Reinforcement
- Gas Stay Reinforcements
All these parts are assembled together to obtain the back door of a car.
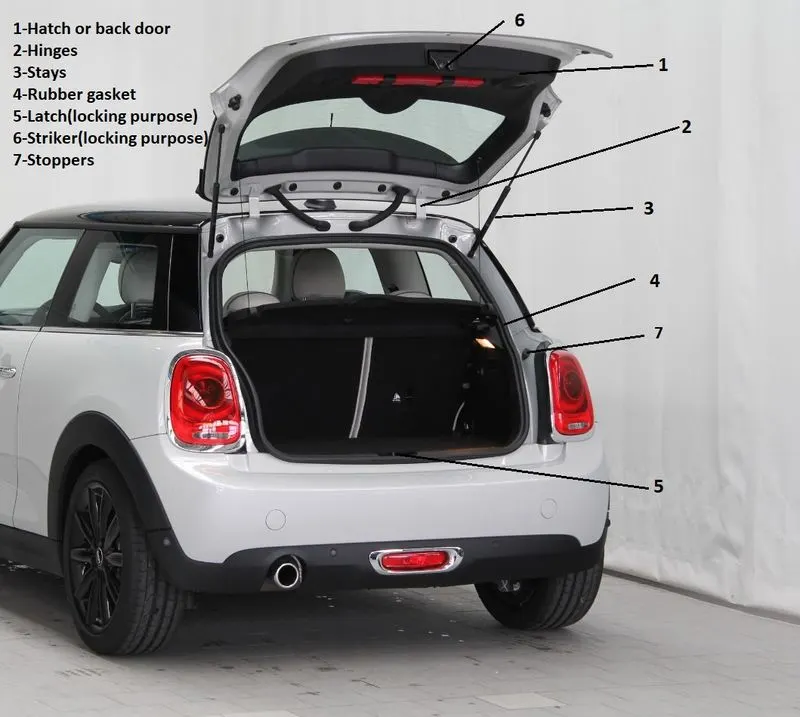
Types of doors based on working position,
- Top Mounted Door
- Side mounted Door
- Bottom Door
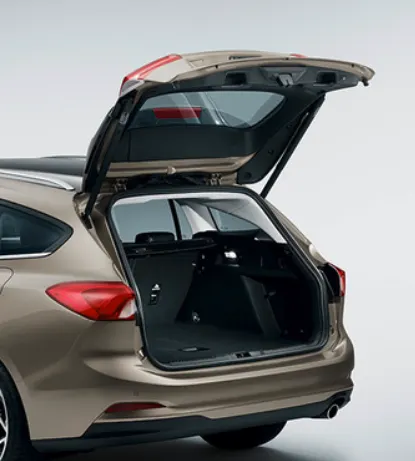
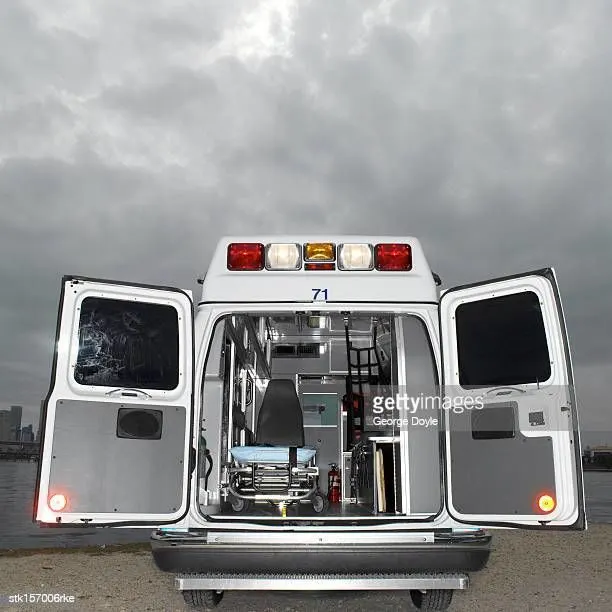
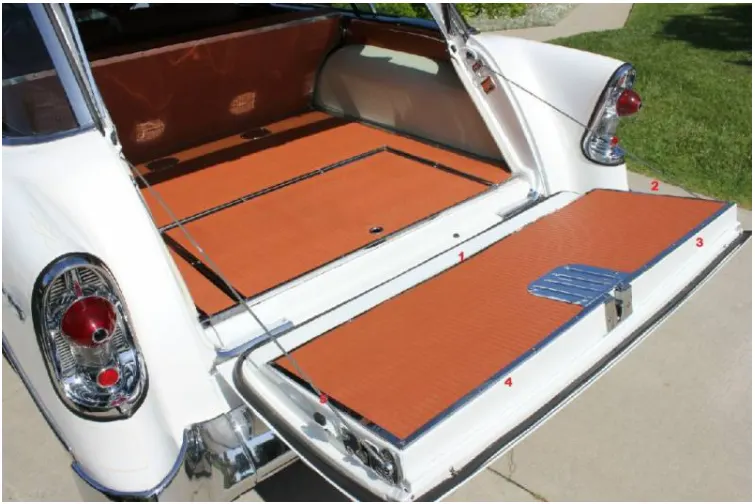
The back door is operated by two types of comodities
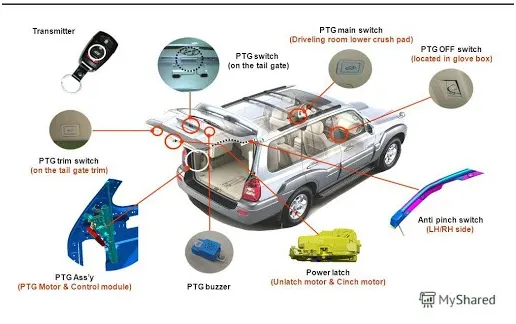
- Power lift system
Power trunk lift system is another sophisticated way of trunk or liftgate opening mechanism which is to automatically open and close of the trunk and release of the latch by the touch of a bottom. Powered trunk Lift system consists of a power latch, anti pinch switch, PTG assly, PTG main switch. When the switch is pressed in the compartment or outside the power latch releases the latch and the entire backdoor is opened. The anti pinch switch is located in order to avoid accidental hand insertion during the operation of the door.
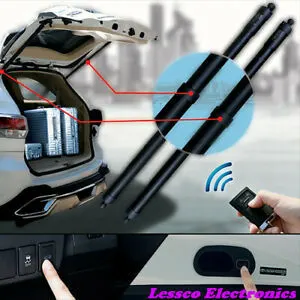
- Gas stray power
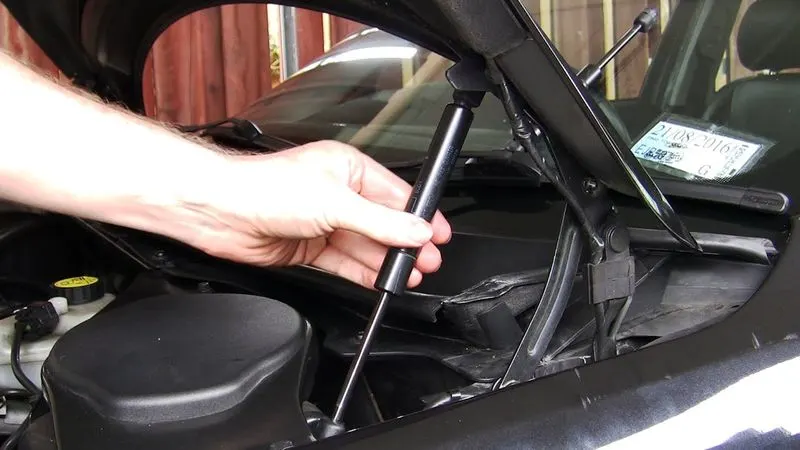
Gas Stay type backdoor is an ideal and most commonly used tailgate mechanism from lower segment car to luxury car segment. The ideal components of tailgate consist of a hinge, door, gas stay and some rubber beadings for sealing of door.
Design Considerations In Back Door Design:
The following are the Design considerations taken while designing the Back Door. They are,
- Visibility Criteria
- Force Dissipation
- Latch and Stricker Positions
- Hinge Position
- Gas Stay Position
- Material Selection
- Space Availability
- Hemming and Relief Areas
All these design considerations go hand in hand with eachother because these positions are dependant on each other and if position gets altered all the positions has to be altered for effective opening and closing of the back door. The Latch and Stricker, Hinge Position and the Gas stay Positions has to be maintained in a proper way so that they play a major role in the opening and closing as well as the rear Visibility criteria of the car.
Material Selection:
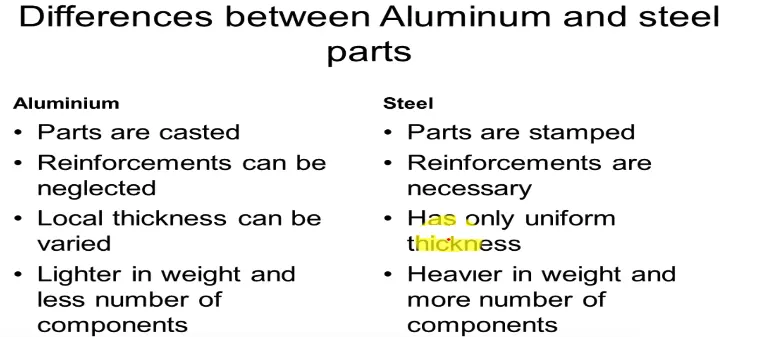
The material selection play a major role in determing the overall weight of the back door. The materials generally used are Steel and Aluminium. The Density of Steel is higher than Aluminium thus it results in adding more weight of the door. Basically the material is used based on the budget of the car, because the cost of steel very cheap than Aluminium. If aluminium is used instead of steel there is no need of many parts like Reinforcements for each mounting and the overall weight geta reduced by 6-10 kg approximately. But the draw back is Aluminium is much costlier than Steel. Hence based on the budget of the car aluminium is used. In higher end models like Benz, Audi, Porshe and BMW we can find aluminium is used instead of steel resulting in reduced weight and increased performance of the vehicle.
Another Factor to make a note is using Casted Aluminium instead of deep drawn Steel components and adding reinforcements to it is the space of the luggage commodity gets increased by a certain amount because the draft angle for Casted aluminium is much lesser (3 degree) than the deep drawn Steel inner panel (7-9 degree). Thus it reduces the space between the inner and outer panel resulting in much larger cabin space than the deep drawn steel inner panel. Thus the material selection is one of the design consideration taken. Since it reduces the space between the inner and the outer panel the rear visibility of the car is also inproved giving more space for the mirror to view.
Hence in this design the material chosen is steel since it is designed for a medium budget car and hence high cost could not be afforded to design the back door.
Different types of Sheetmetal operations are done in the Back Door
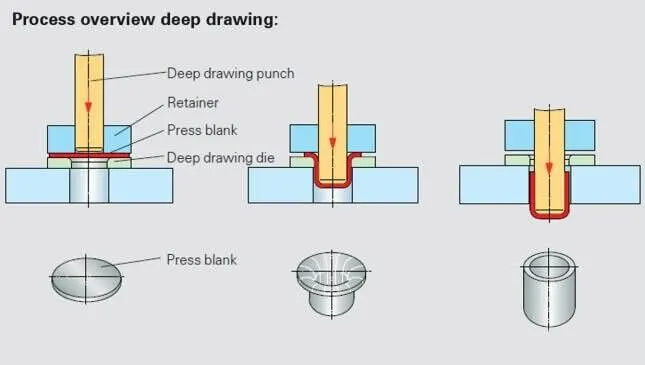
Deep Drawing:
The metal deep drawing process is an effective method of manufacturing of cups, cans and other similar deep drawing products. The deep drawings having two main categories.
- First- stage drawing: The blank shape of metal is placed on the die and contact with the punch. When the metal specimen is flat piece of sheet metal used in forming and finish the product. Initially the punch moves in downward direction. The outer rim of blank is subjected to pure radial drawing (drawing toward in vertical axes) between die and blank metal. The metal become a bend and sliding over die and also stretched between die and punch. The metal in vicinity of punch head and contact with it bend and slide over radii and stretch over punch head.
- Redrawing: The components drawn from first stage again it is redrawn convert into more depth to form a cup shape in the die and punch. The second stage of drawing is called as redrawing
Embossing:
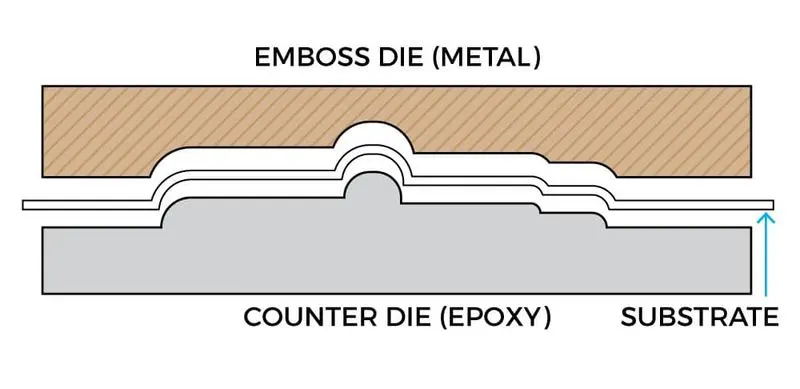
Embossing is a metal forming process for producing raised or sunken designs or relief in sheet materials by means of matched male and female roller dies, theoretically with no change in metal thickness or by-passing sheet or a strip of metal between rolls of the desired pattern. Metal sheet is drawn through the male and female roller dies producing a pattern or design on the metal sheet. Depending on the roller dies used, different patterns can be produced on the metal sheet.
Materials commonly used in the metal embossing process include:
- Aluminum alloys
- Steel alloys
- Zinc
- Copper
- Galvanized steel
- Brass
- Cold rolled steel
Blanking:
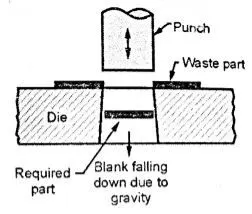
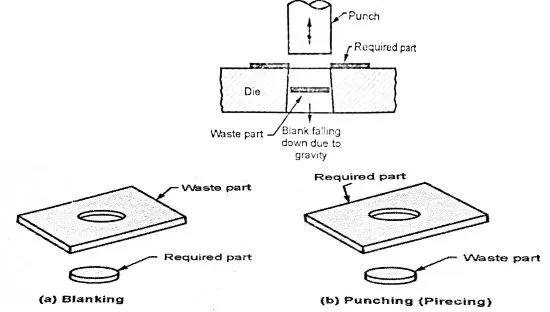
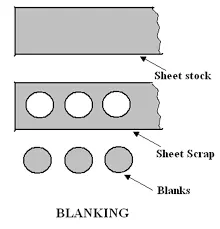
Blanking is a cutting operation of a flat metal sheet and the article punched out is known as blank. Blank is the required product of the operation and the metal left behind is considered as a waste.
Punching:
It is similar to blanking only the main difference is that, the hole is the required product and the material punched out from the hole is considered as a waste.
MOUNTING
HEMMING
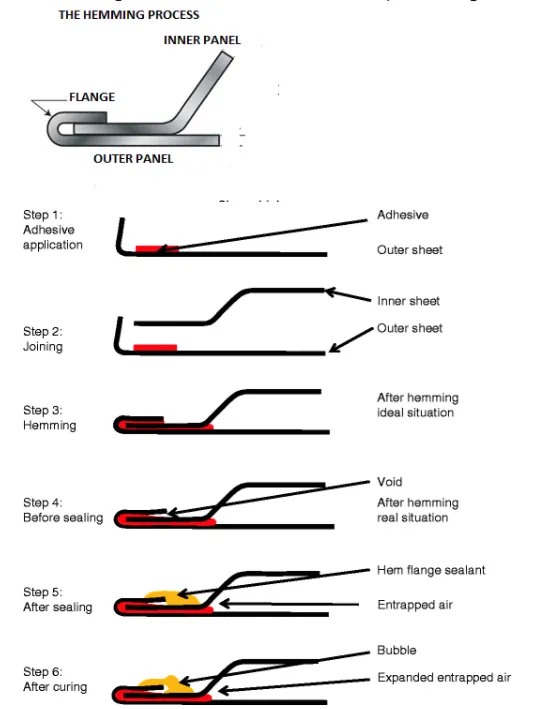
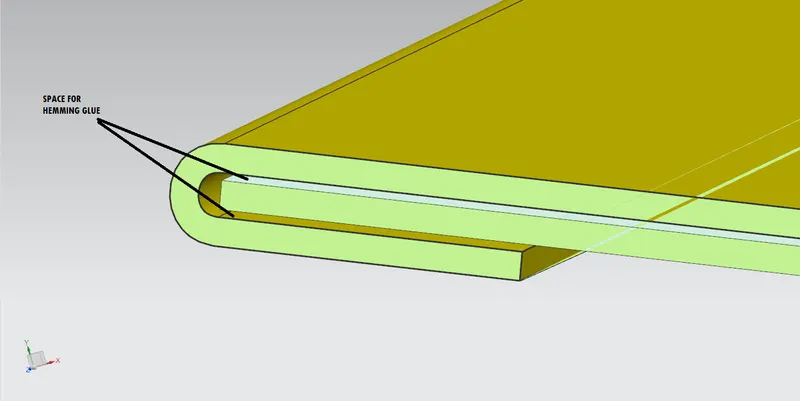
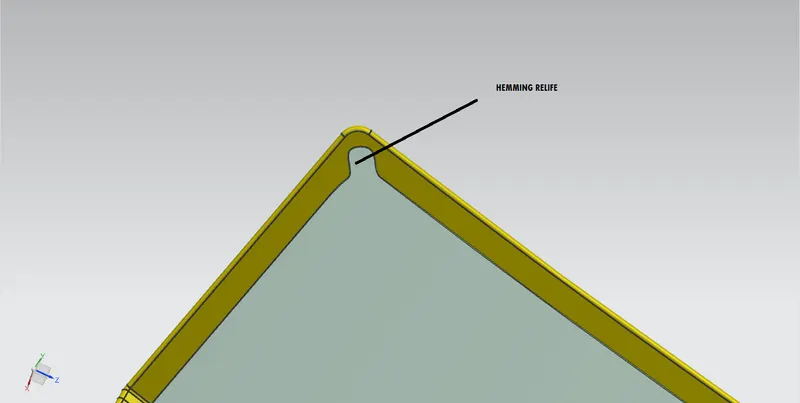
Hemming and Seaming are two similar metal working processes in which sheetmetal edge is rolled onto itself.Hemming is the process in which the edge is rolled flush to itself, while a seam joins the edge of two materials. The Hemming is done on the outer and the inner panel with an clearance of 0.2mm on the either sides. Since at the corners the hemming is difficult to perform, clerances has been given at the ends of panels so that it would for the hemming operstion is performed. Here is the image of the hemming relief at the corners.
REINFORCEMENT
TRAJACTORY FOR LATCH AND STRIKER
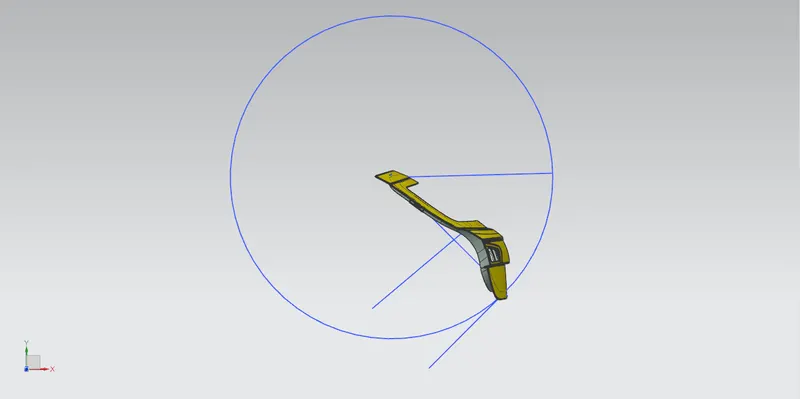
The Latch and Stricker positions play a major role in determing the opening and closing of the back door. Hence the opening and closing of the had to smooth and inorder to ensure that the the centre point of the latch and stricker has to to be at the same point and the trajectory has to be tangent to the open close circle that is drawn. This is shown in the below image. Only if the centre points and the tangent line are perfect the opening and closing of the back door is smooth and clear. Or else the Hinge positions, Gas stay positions and Latch and Stricker Positions has to be altered to meet the change.
ASSEMBLY
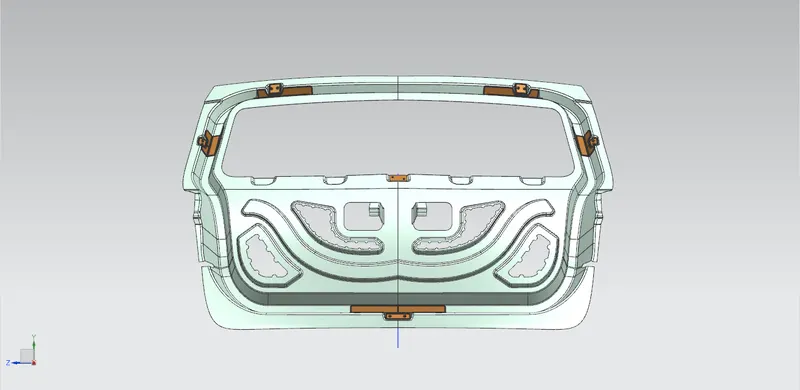
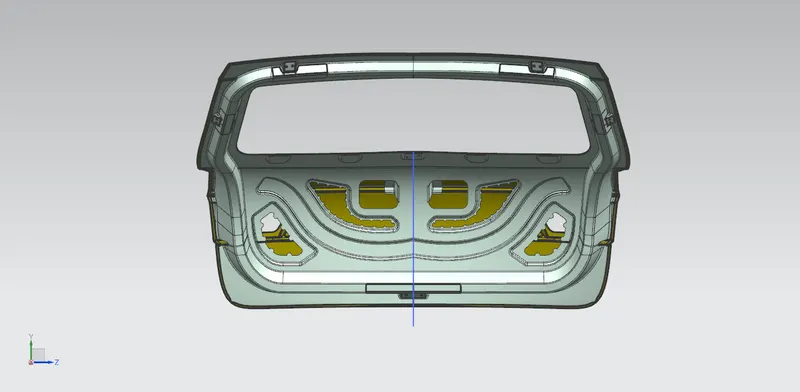
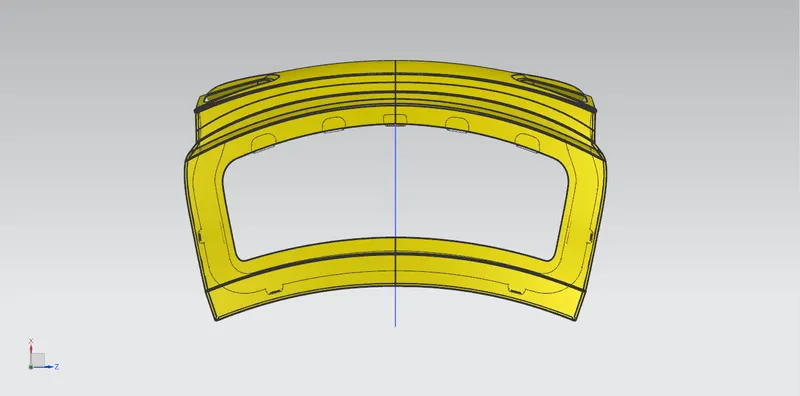
DRAFT ANALYSIS OF INNERPANEL
The draft analysis technique is used to analyze whether our part model created in CAD is manufacturable based on the draft condition applied. Here the part should get easily removed from the panel dies (in case of Sheet metal part) or Mold (in case of plastic).