Design of backdoor
AUTOMOTIVE DESIGN OF CAR BACK DOOR
Objective:
- Use the provided styling surface to come up with a back door design, use appropriate design methodologies and provide the necessary reinforcements and embosses.
- Report Develop a detailed report for the Back door design by explaining the design methodologies and about the components developed in the design
- Draft Analysis Perform Draft Analysis along the tooling direction
Tool Used:
Siemens NX CAD (Unigraphics)
Introduction:
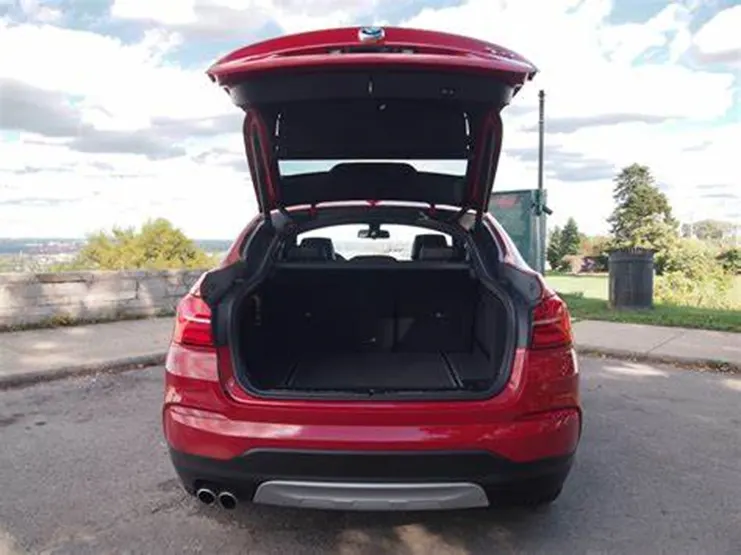
- A passenger car is a wheeled motor vehicle used for transporting passengers, which also carries its own engine or motor. The Back Door or hatchback or tailgate of a car is the rearmost part of the vehicle which gives access to the trunk space of the vehicle. The rear door also supports the reinforcements and added weights of the Wiper Motor, Gas Stay, Tail Lamp, and Latch and Striker.
- The Backdoor/tailgate is one of the closure commodities in BIW sheet matel design. The backdoor has a lot of components inside and is designed to incorporate them easily. It affects the rear visibility and luggage area.
- The material used for door manufacturing depends on the budget and performance of the vehicle. Mostly Steel and Aluminium will be used whereas low-budget vehicles use Steel which makes the manufacturing process easy and cost-efficient since it follows the Stamping of Moulds.
Major Parts:
The backdoor consists of the following basic components:
- Backdoor Outer Panel (Upper)
- Backdoor Outer Panel (Lower)
- Backdoor Inner Panel
- Hinge Reinforcements (LH & RH)
- Gas-Stay Reinforcements (LH & RH)
- Latch and Striker Reinforcement
- Wiper motor Reinforcement
Design Consideration of a Backdoor:
The intent of the project is to design a BIW Back Door of the vehicle considering the engineering standards and manufacturing requirements which satisfies the Deep Drawing Process.
- Functional Requirement of Hinge and gas stay
- Rear visibility criteria
- Boot Space and accessibility
- Rear Crash Regulation
- Gap and flushness Requirements
Impotence Of material choosing:
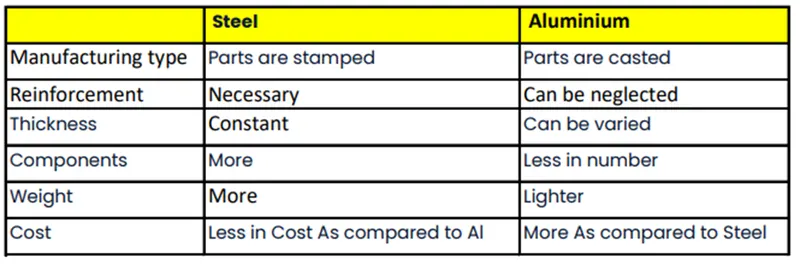
- The car parts are made of Steel or Aluminium based on the budget of the car.
- Using Aluminium improve the Strength where we can avoid the reinforcements.
- Aluminium parts are casted and we can vary the thickness of the part, because of this avoid or reduce the number of parts as compared to Steel.
- Only drawback is the cost of aluminium, which is high cast As compared to steel.
- Steel Parts are stamped, we cannot vary the thickness of the part because of a greater number of parts are added. which could increase the weight of the part.
- So now a days most of the car manufacturers are trying to use Aluminium instead of Steel and they reduce the number of parts and weight of the car drastically.
Manufacturing Operations Involved:
- Deep Drawing
- Stamping
- Punching & Blanking
Deep Drawing:
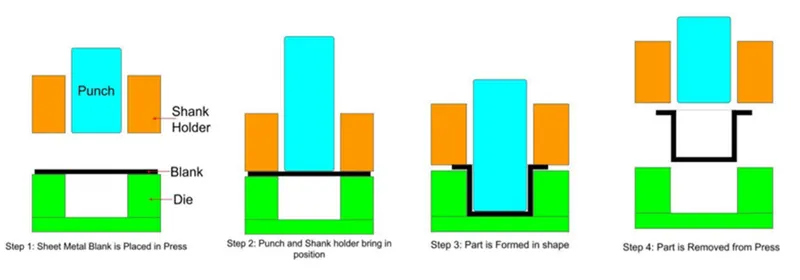
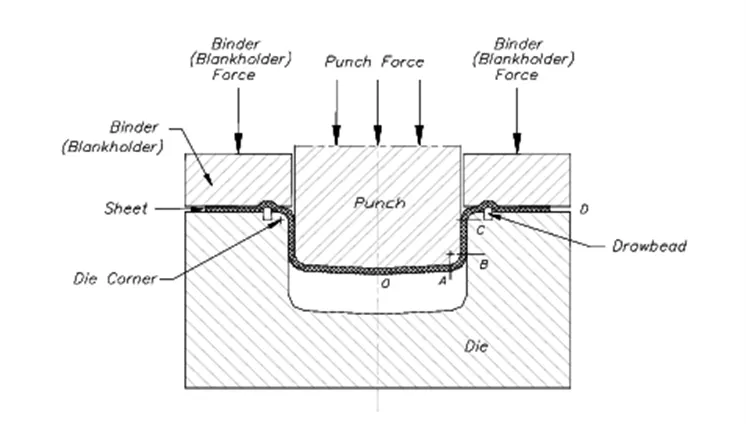
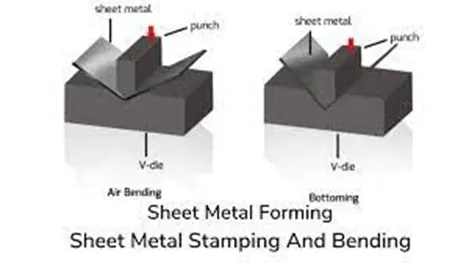
It is a sheet metal forming process in which sheet metal blank is radially drawn into a forming die with a punch, when the depth of part exceeds its diameter then it is considered as deep drawing.
Stamping:
The process of turning sheets of metal into a useful part or component is called sheet metal stamping. The metal is fed into a press, where the stamping tool, also known as a die, creates the desired shape. The die is pressed into or through the metal with tremendous force.
Punching & Blanking:
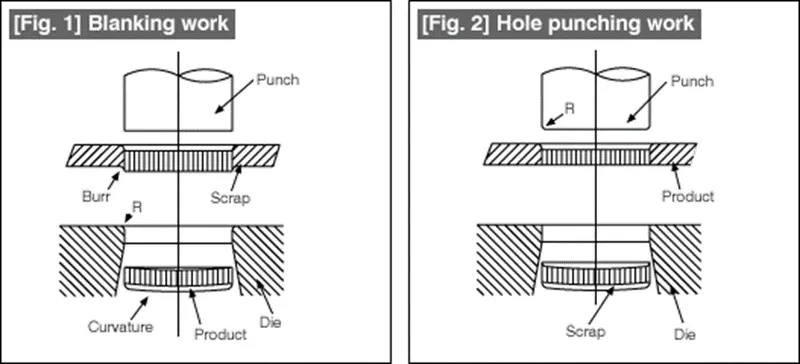
Both blanking and punching are material forming processes that involve the precise removal of material from a workpiece. The main difference between the two processes lies in the end product produced.
In blanking operations, the final part or product is punched-out of the larger sheet material, with the remaining material being discarded as scrap. On the other hand, in punching operations, the material removed is discarded, and the final product is the remaining material which then undergoes further processing.
Joining Processes used in Backdoor assembly:
There are different joining processes that are used in the assembly of backdoor such as hemming, spot welding etc.
Hemming Process:
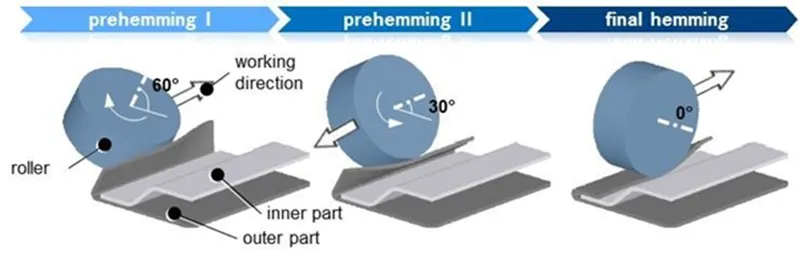
It is a forming operation in which the edges of the sheet are folded or folded over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
In-car part production, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Typical parts for this type of assembly are hoods, doors, trunk lids and fenders.
Spot Welding:
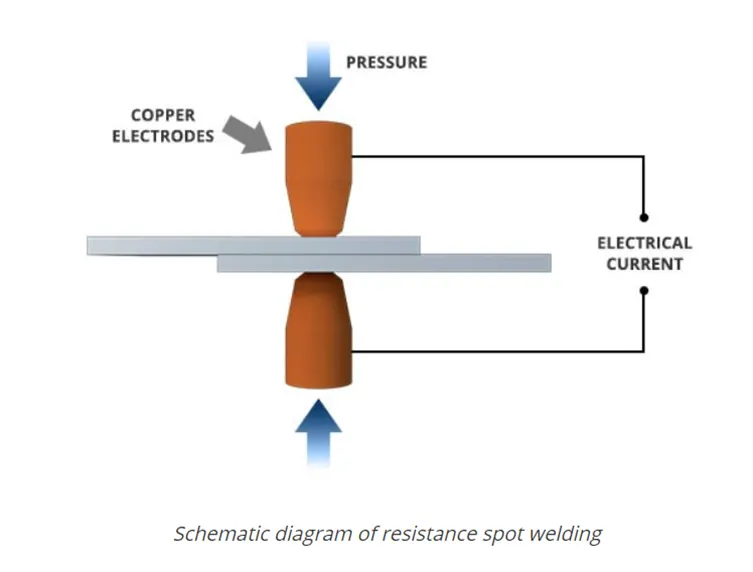
A form of resistance welding, spot welding is one of the oldest welding processes whereby two or more sheets of metal are welded together without the use of any filler material.
The process involves applying pressure and heat to the weld area using shaped alloy copper electrodes which convey an electrical current through the weld pieces. The material melts, fusing the parts together at which point the current is turned off, pressure from the electrodes is maintained and the molten “nugget” solidifies to form the joint.
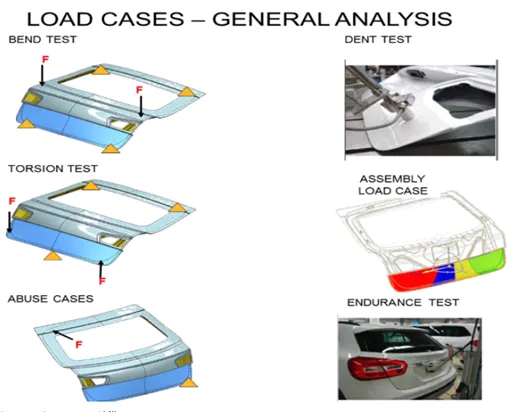
General analysis on car tail gate:
- Bend Test
- Torsion Test
- Abuse Test
- Endurance Test
- Deny Test
- Assembly Load Test
Design Of Backdoor Outer Panel:
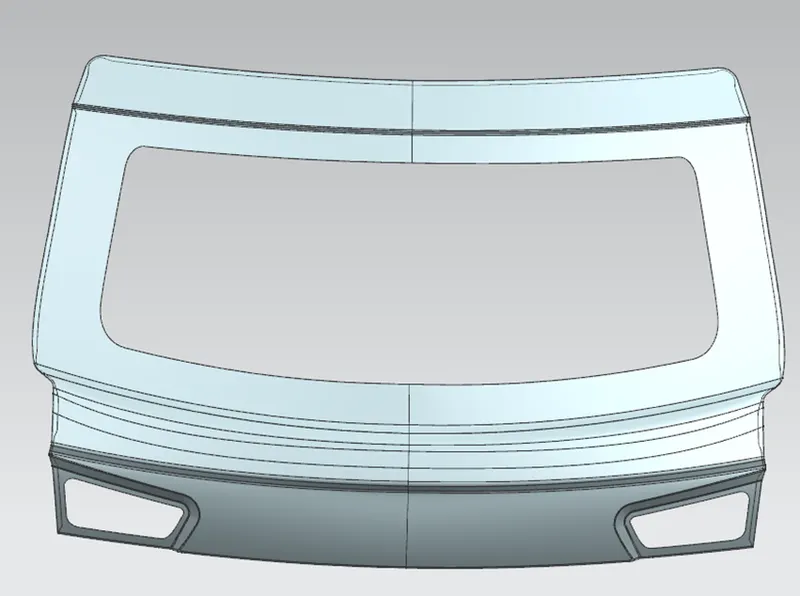
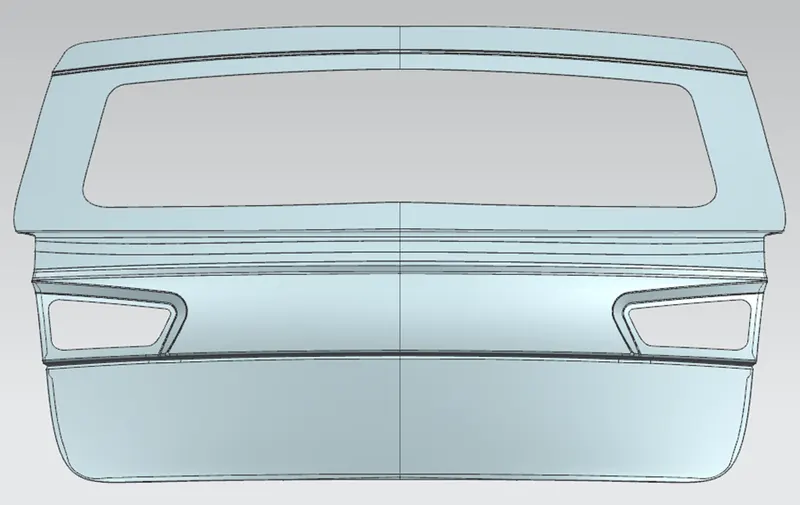
The Outer Panel is the styling surface of the back door. Other components of the backdoor are designed with reference to the outer panel. It acts as the outer cover and deals with the aesthetics of the car.
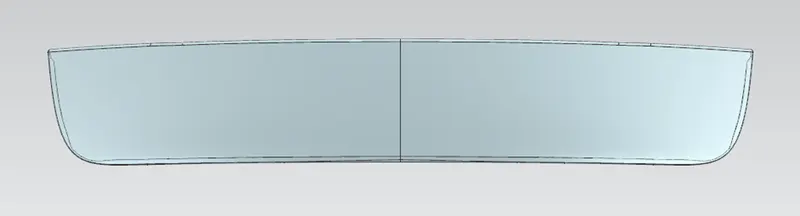
In this design outer panel is divided into two parts
- Outer Upper Panel
- Outer Lower Panel
Outer Upper Panel:
The outer panel is the styling surface of the source of the design of other parts of the back door. The outer panel should be designed with the requirement of tail light, rear glass and also the crash test requirement. The outer panel should be designed in an attractive way because it gives the rear external shape of the car. It acts as the cover outer and deals with the aesthetics of the car.
Outer Lower Panel:
Outer Upper & Lower Panel:
Tooling Direction:
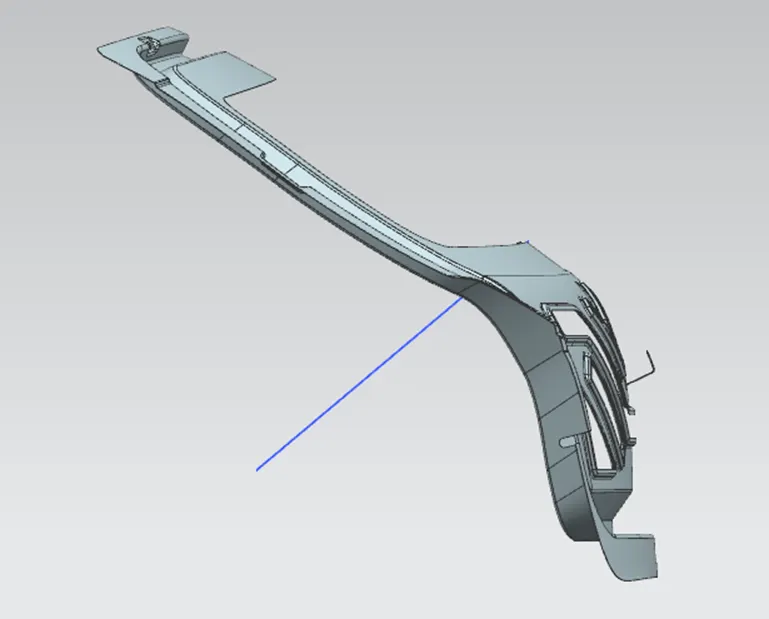
- Before starting to design the inner panel of the back door the tooling direction for Deep Drawing purpose should be created.
- Then the styling surface needs to be checked and analysed since it might have irregularities, hence it must be fixed first.
- Then the back door was designed using the top-down approach.
Design of Backdoor Inner Panel:
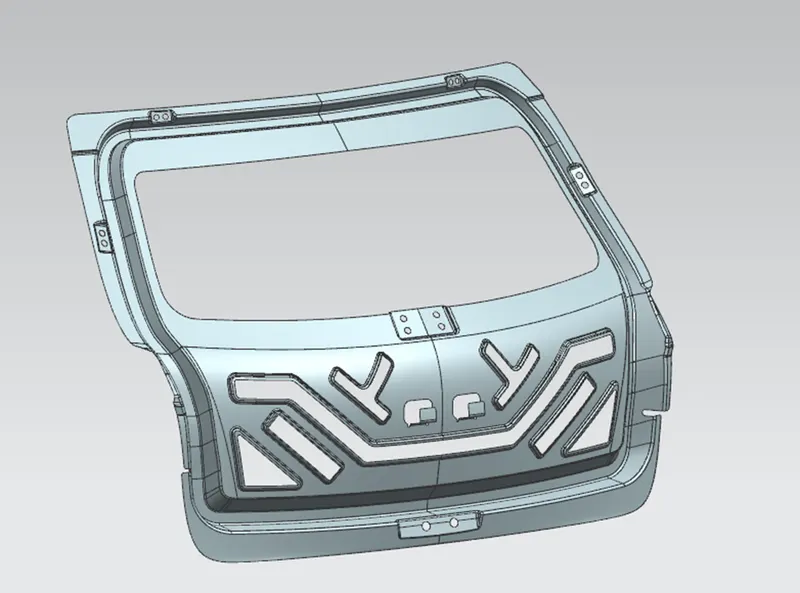
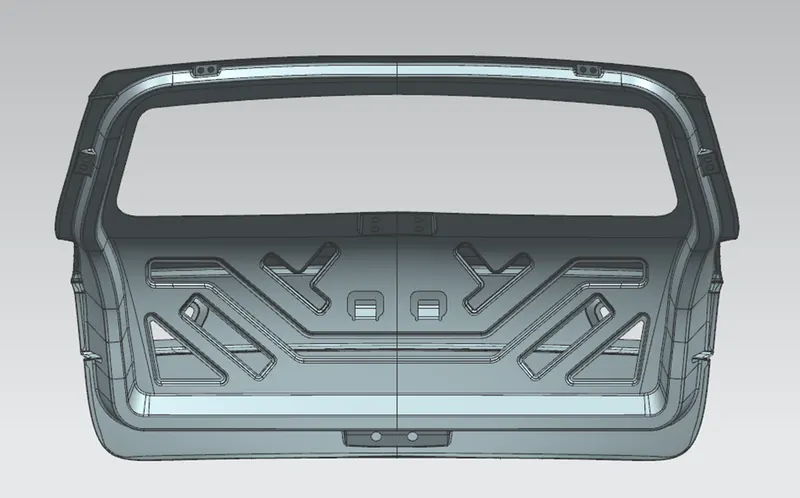
After creating the tooling direction, the design of the inner panel will begin where we will first develop an effective sealing flange by checking all the boundaries and by following the shape of the inner panel design. By creating multiple flanges and by using surface modelling techniques the concept design of the inner panel was created.
- After the concept of the inner panel is developed, then the child components like a hinge, latch, gas-stay locations, and their reinforcements must be designed. Which completes the overall design of the tailgate.
- The embosses were created in ‘V-Shape or Y-Shape’ so that if the vehicle undergoes the crash, then the force dissipates over it which reduces the damage transferred to the trunk space.
Mastic Sealant:
The mastic sealant is used to fix the inner panel with the outer panel which increases the NVH factor and stiffness of the back door.
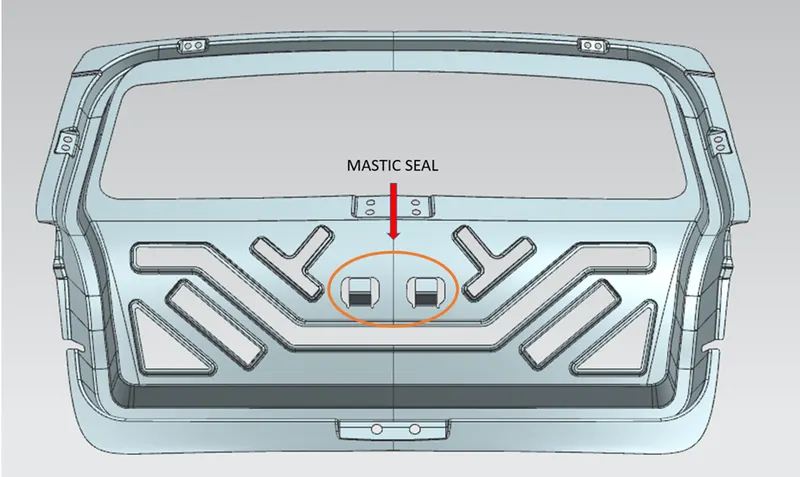
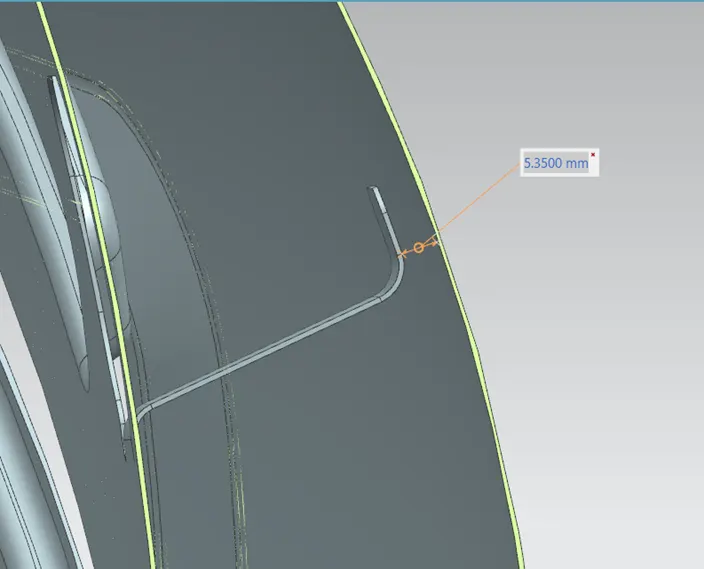
Minimum gap 5 mm between mastic sealant and outer panel.
Hinge, Gas Stay & Wiper Motor Emboss:
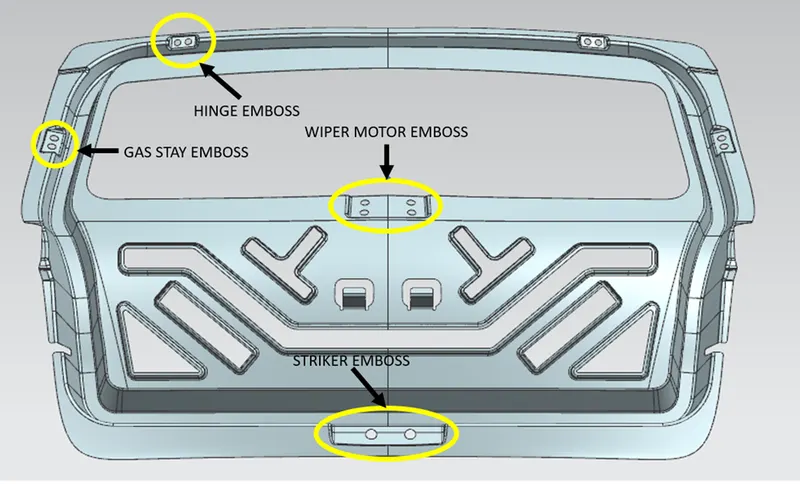
The Orange circle denotes the hinge emboss which was created using the datum plane and emboss feature in NX. It was also designed in a way that the emboss should have a flat surface for assembling the hinges using it.
The violet circle denotes the gas stay emboss which was created using the surface of the connecting flange.
The yellow circle denotes the Wiper motor emboss which was created using the surface of the connecting flange.
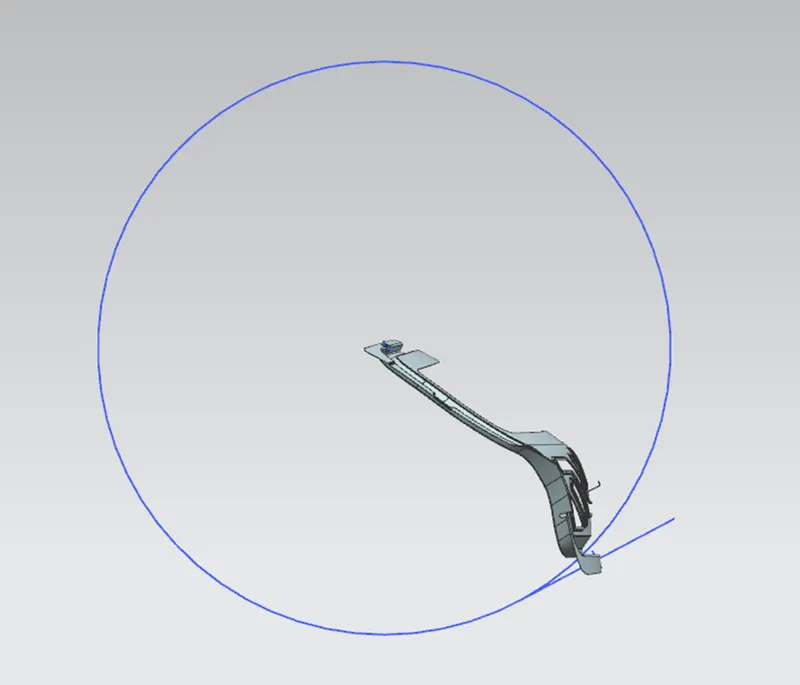
The Latch and Striker emboss were designed by creating a trajectory that follows the opening and closing of the back door with respect to the hinge axis.
STRIKER POSITION:
The position of the hinge should be perpendicular to the latch when the latch and striker meets. The circle is drawn from the centre of the hinge axis to find the path of the striker and positioned perpendicular to the path.
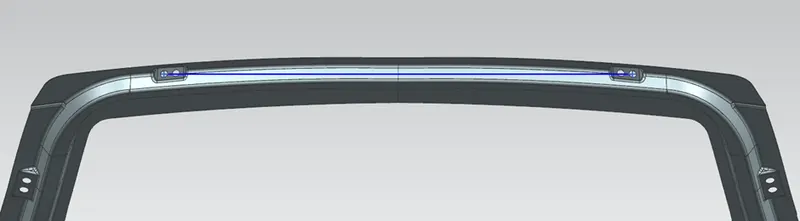
Hinge axis
HEMMING:
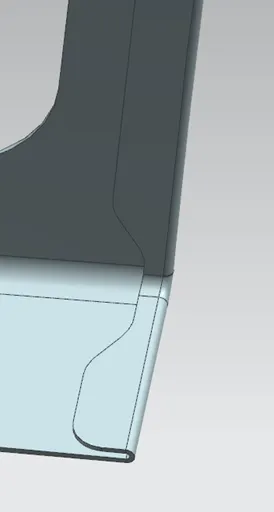
Hemming and seaming are two similar metalworking processes in which a sheet metal edge is rolled over onto itself. Hemming is the process in which the edge is rolled flush to itself.
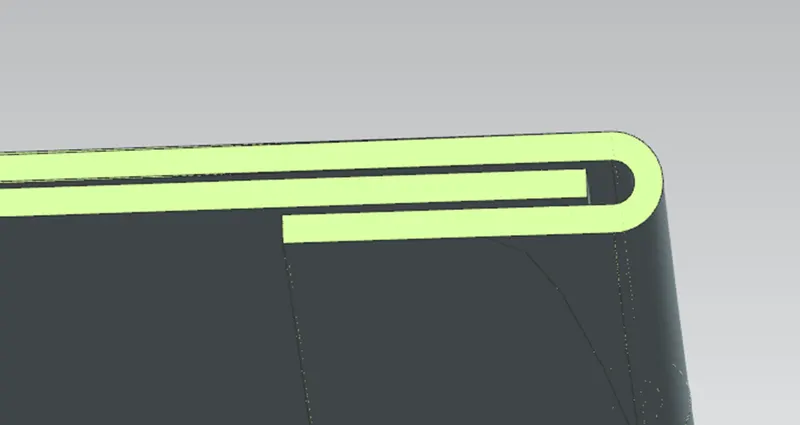
- The outer panel was designed as two separate parts named as outer panel upper and outer panel lower.
- After designing the outer panel the Hemming was created by offsetting the surface with the help of face blend and swept surface.
- The two separate outer panels will be joined using Blanking
CORNER RELIEF:
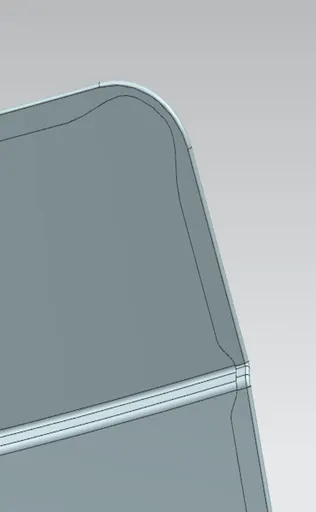
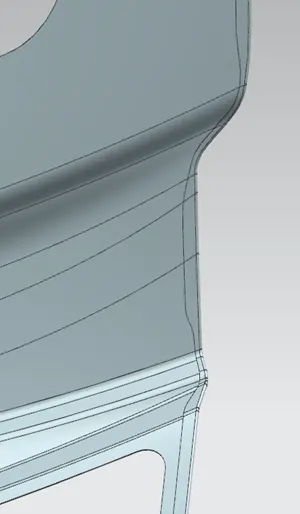
During the hemming process, when giving the Corner Relief helps to control sheet metal material behaviour and to prevent unwanted deformation during unbend operations and also helps to reduce the number of passes in hemming.
DESIGNING THE REINFORCEMENTS:
The thickness provided for all reinforcements is 1.5 mm.
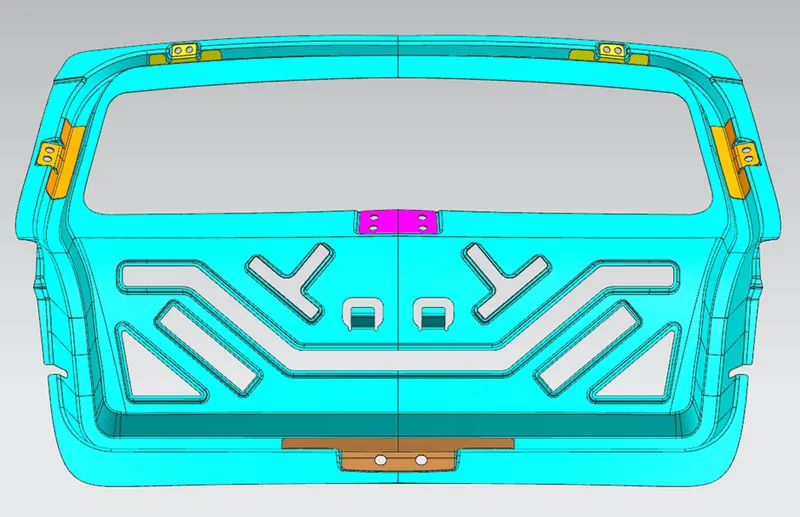
- Hinge Reinforcement
- Gas Stay Reinforcement
- Wiper Motor Reinforcement
- Latch Reinforcement
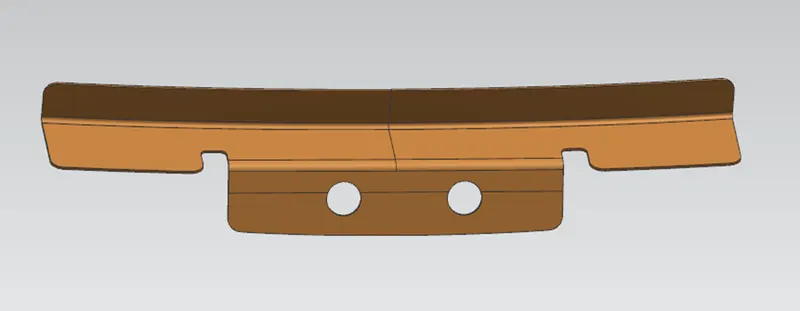
All the reinforcements were created using the same method, first, the linked body was created separately for each with the help of extract geometry and then the required portion was trimmed out and then thickened.
Hinge reinforcement:
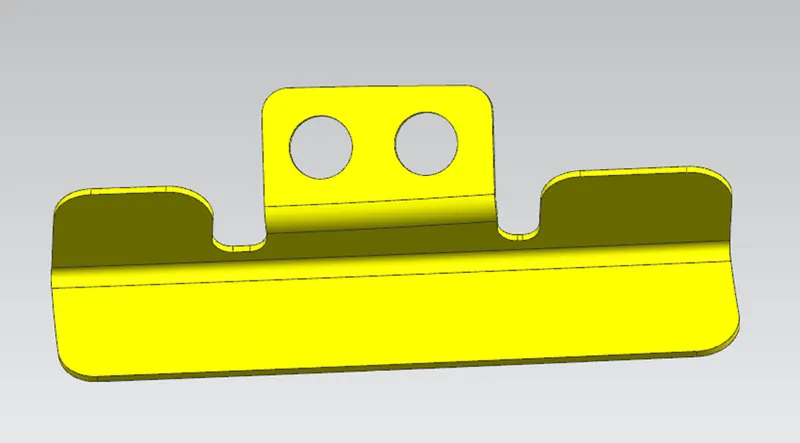
Hinges enable the opening and closing of the back door. One end of the hinge is fixed on the backdoor and the other end on the Roof, on both sides. Hinges can be placed outside or inside the backdoor.
The hinge reinforcements are added to compensate for the weak region due to the acting load over it.
Gas Stay Reinforcement:
Gas Stay is a device used for supporting the back door in its open position. Gas stay requires no manpower and is engaged into support position automatically as the back door opens. One end of the Gas Stay is fixed on the backdoor and the other end on the Body Side or on the Back door stationary area.
Embossing is provided at the Gas Stay mounting area to compensate for weakness and improve strength.
Wiper Motor Reinforcement:
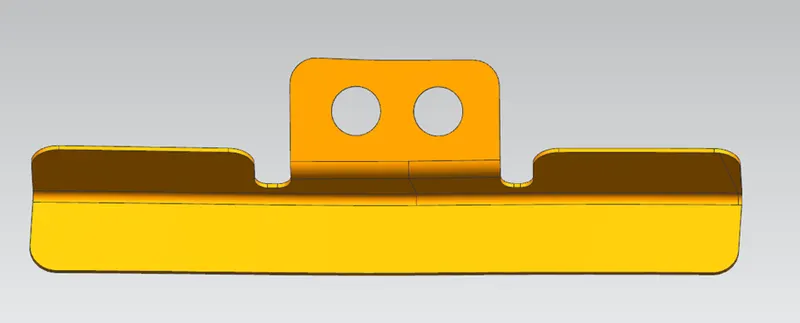
Wiper motor reinforcement is created to mount the wiper motor assembly.
Latch and Striker Reinforcement:
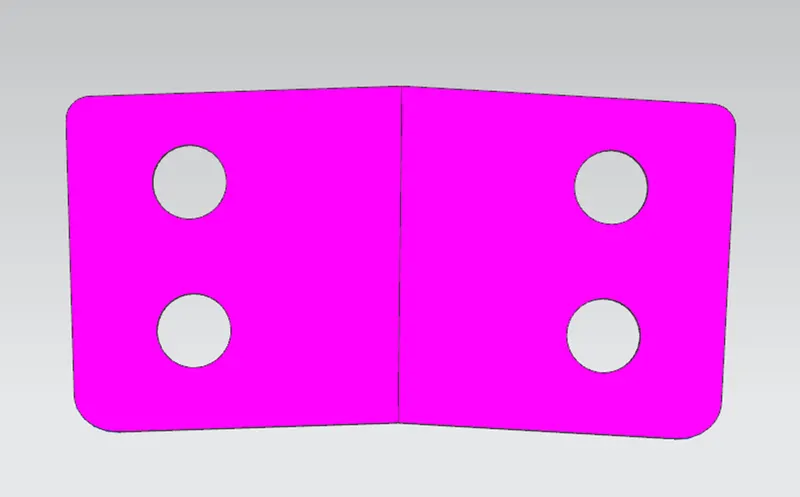
The Latch & Striker forms the locking mechanism of the backdoor with the car. Due to regular opening, closing, and over slamming of the backdoor, there is stress developed in the Latch and Striker area. To compensate for the same, reinforcements are added in this area.
DRAFT ANALYSIS:
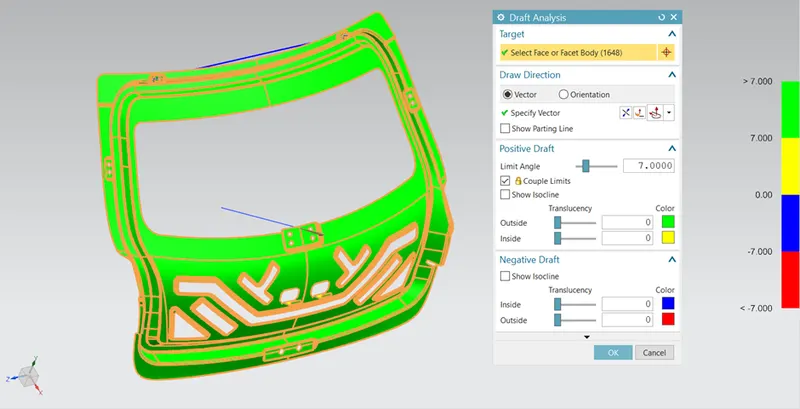
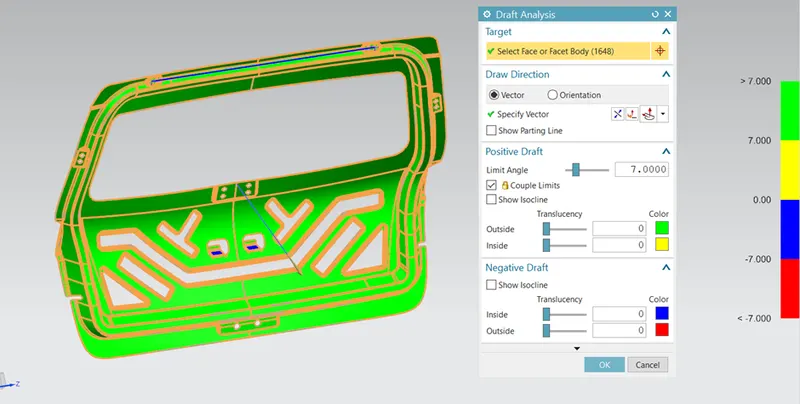
- The draft analysis will be performed for the tooling direction created at first and checked that the model is suitable for manufacturing.
- Then to get a complete green portion the necessary changes to the draft angle of the embosses were carried out by optimizing the model.
- The Draft Analysis command enables us to detect that the part drafted will be easily removed or not.
- This type of analysis is performed based on color ranges identifying zones on the analyzed element where the deviation from the draft direction at any point, corresponds to specified values.
Views of the designed Back Door:
Front view:
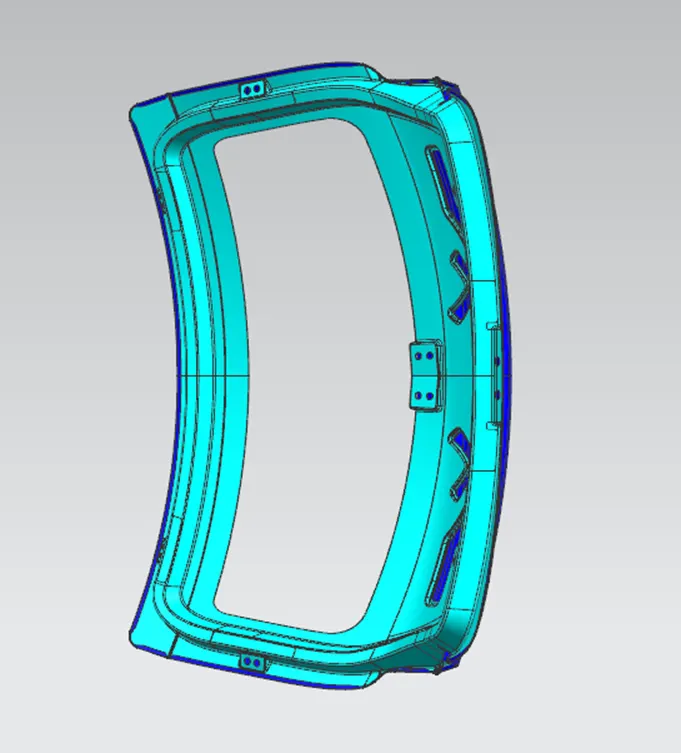
Top view:
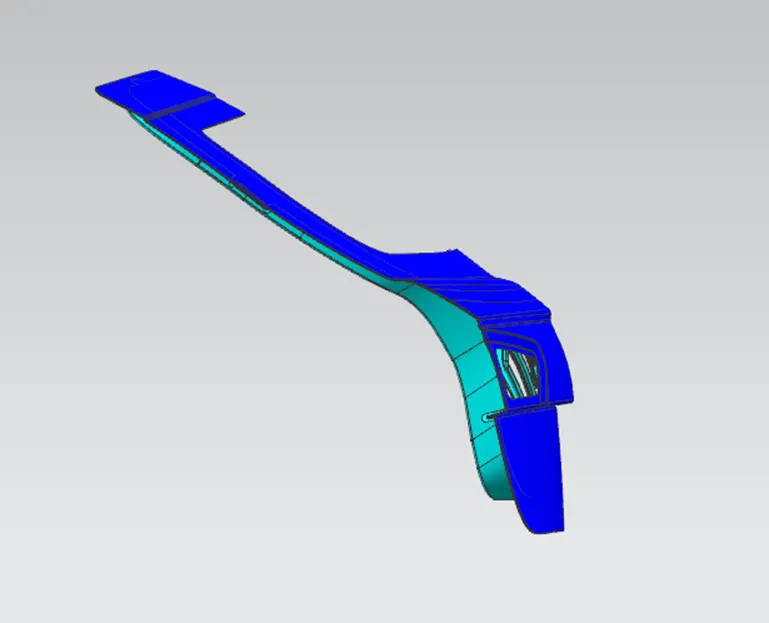
Left Side views:
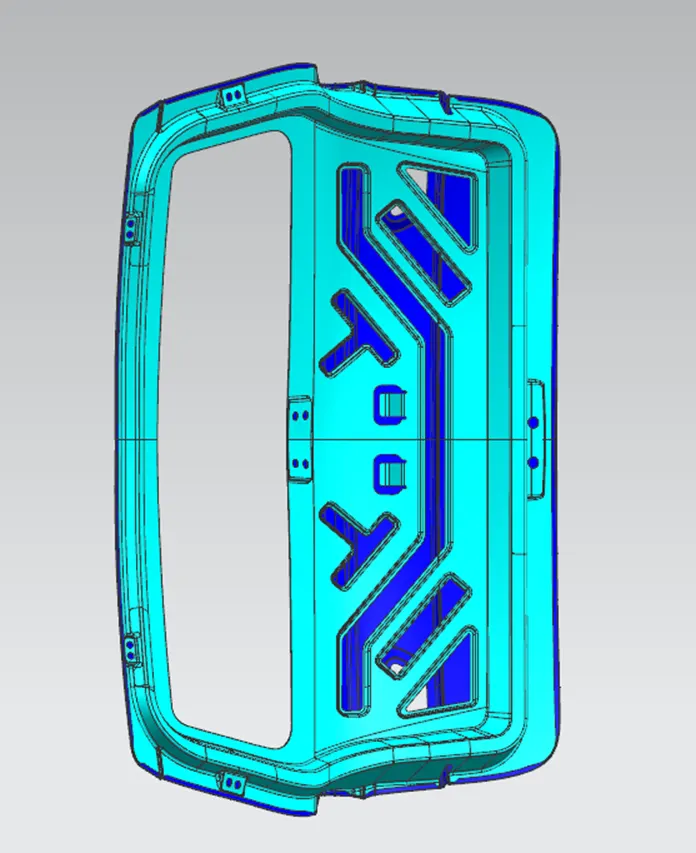
Right Side views:
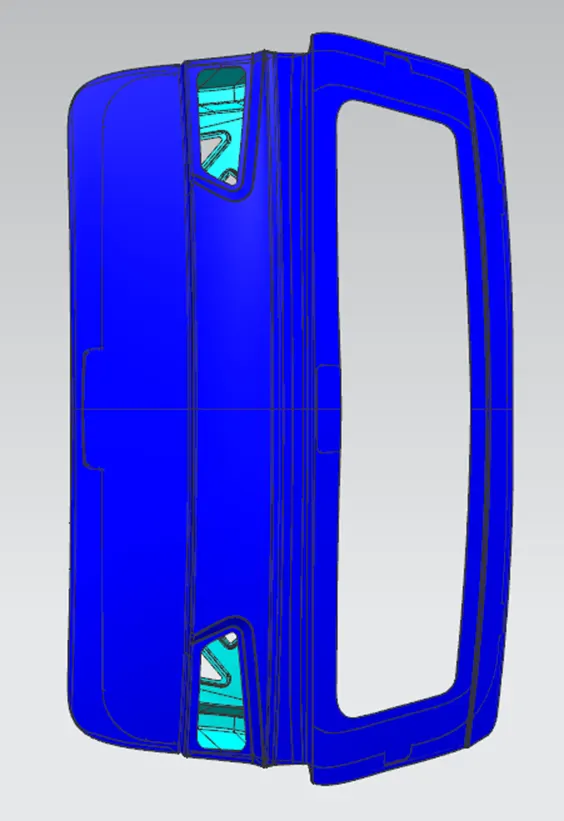
Isometric View:
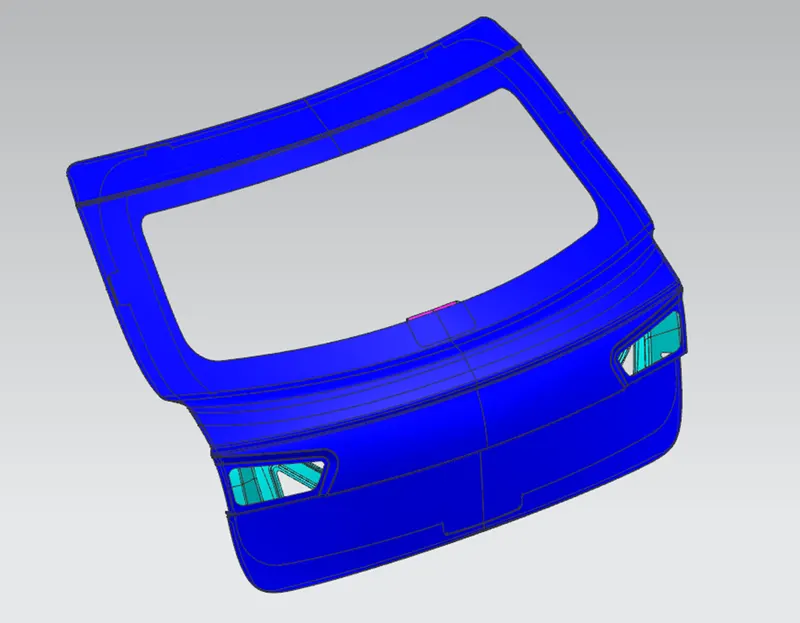
CONCLUSION:
Thus, the BIW Back Door of a car was designed following the engineering standards and also the deep drawing requirements were satisfied.