Week 9 - Project 1 - Door Trim Lower with Engineering Features
DOOR TRIM LOWER
Aim: To Create the Door trim lower component through the given Class-A surface.
Objectives:
• Creation of Tooling axis with appropriate draft angle.
• Creation of other surfaces (eg, B and C surfaces) for creating a solid component. • Perform Draft analysis on Class A surface and Solid model hence created.
Draft
The draft is the amount of taper for moulded or cast parts perpendicular to the parting. line. Draft angles are a design consideration that makes it much easier for a part to release cleanly from a mould. A draft angle is calculated as a degree measurement (or, less often, an inch or millimetre measurement) from the vertical axis of a mould, and it helps account for thermoplastic shrinkage, a practical reality of the injection moulding process for most materials.
Draft angles are generally a requirement of injection moulding design (though there are a select few soft materials, like nylon, that can get away with draft angles of zero). The draft should be a part of the design for manufacture, and all stakeholders and contributors should be aware of its need at the outset of the design process. This includes product designers, design engineers etc and this allows considerations for design requirements to be taken into account. Any draft is always better than no draft.
Importance of Draft:
By accounting for thermoplastic shrinkage during the cooling process, draft angles significantly reduce friction between the finished, cooled part and the side of the mould, Not only does this create a much easier release process, but it also offers several other benefits, depending on the design of the part which is as follows:
• Reduces the chance of damage to the part due to friction during the release.
• Reduces wear and tear and chances of damage to the mould.
• Ensures a uniform, smooth, unscratched finish when required. • Ensures the integrity and uniformity of other surface finishes and textures.
• Reduces overall cooling time by lessening or eliminating the need for unconventional ejection setups.
• Most, if not all, of these benefits, offer either direct or indirect overall production cost reductions.
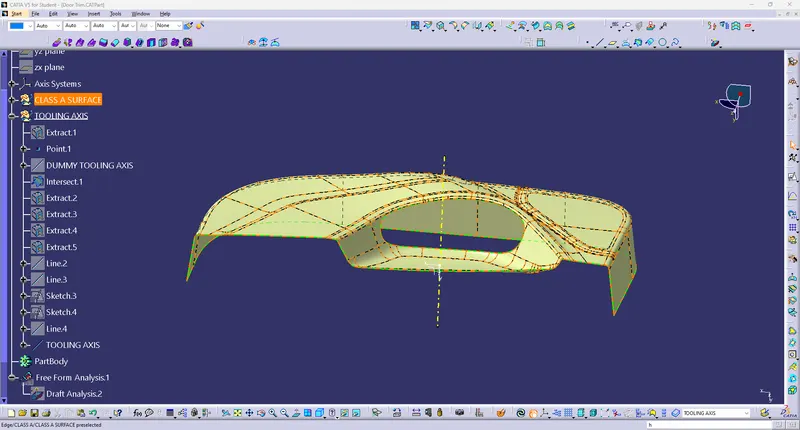
Given CLASS A SURFACE:
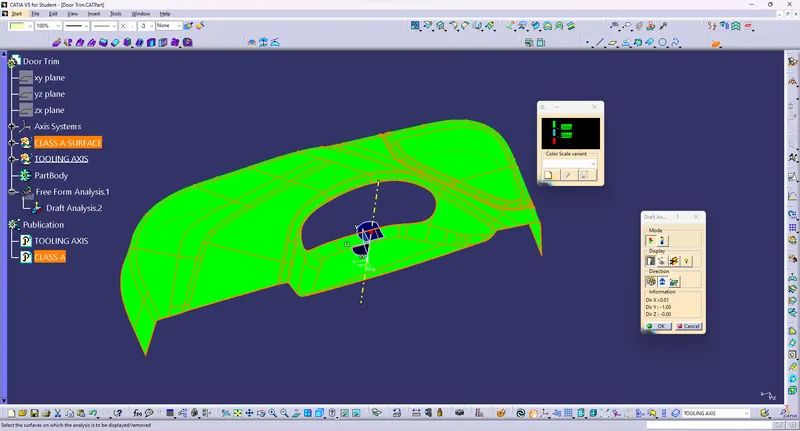
Creation of Tooling Direction:
TOOLING AXIS:
By taking into account this tooling axis, the draught angle that is required to be provided is nothing more than the direction in which the mould opens and shuts. The bisecting technique allows us to make a tooling axis.
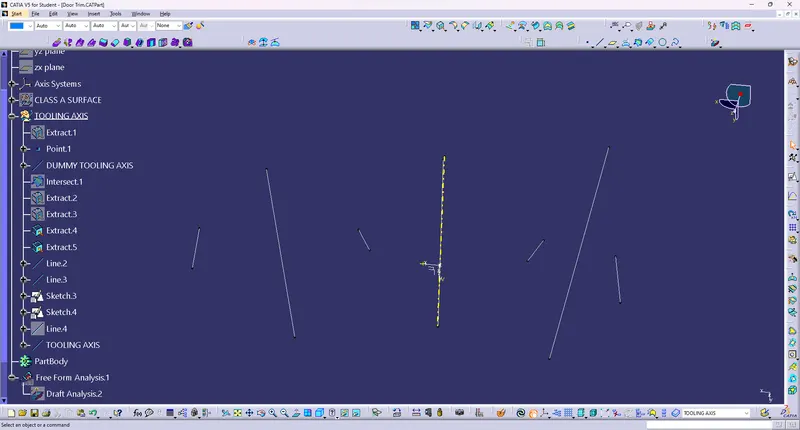
BISECTING METHOD:
This technique is used to generate tooling axes for that purpose. First, the direction of moulding must be decided. Next, a dummy tooling axis is created for the purpose of reference.With this approach, we pick the surfaces that could cause issues and consider intersections in the x and y directions. Using these curves, we create two lines, from which we create a bisecting line in both the x and y directions.Tooling axis cleaning x-direction and tooling axis clearing y-direction are the terms used to describe how the clearing is carried out.
DRAFT ANALYSIS:
DRAFT:
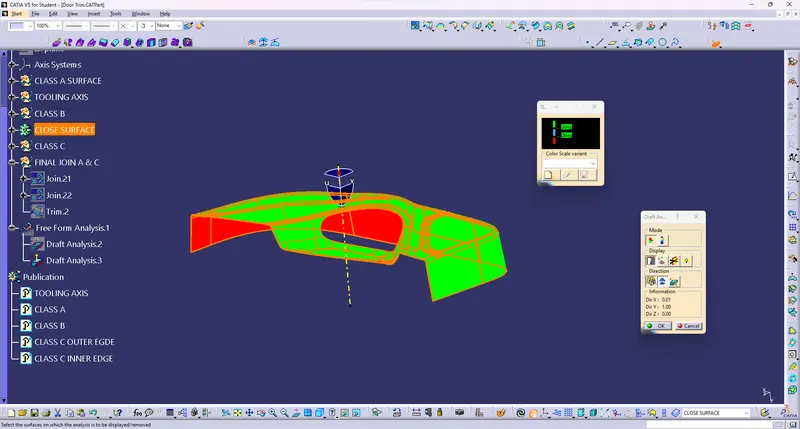
Draft angle is nothing more than giving the part a tapered area for simple release from the mould during manufacture. This is notably done when designing plastic components with complicated shapes. Although it typically has a 3-degree draught angle, it can change depending on the component that needs to be constructed.
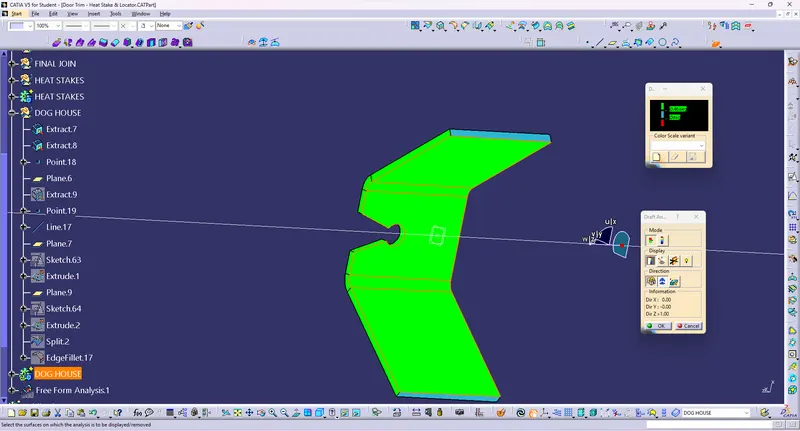
DOG HOUSE DRAFT (SIDE CORE)
FINAL DRAFT
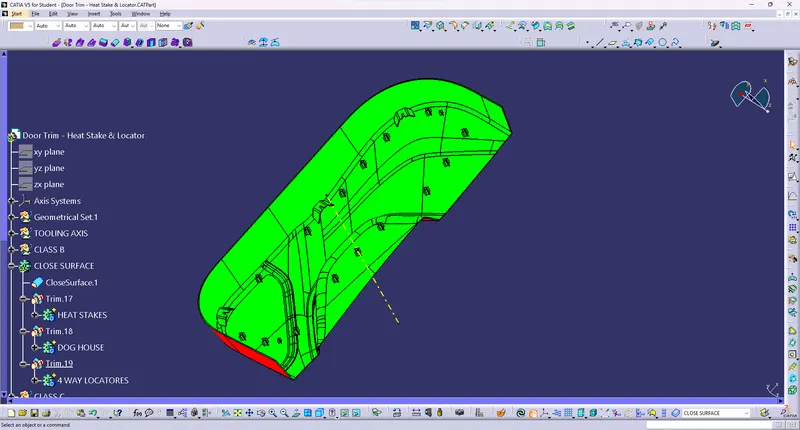
RIB DRAFT
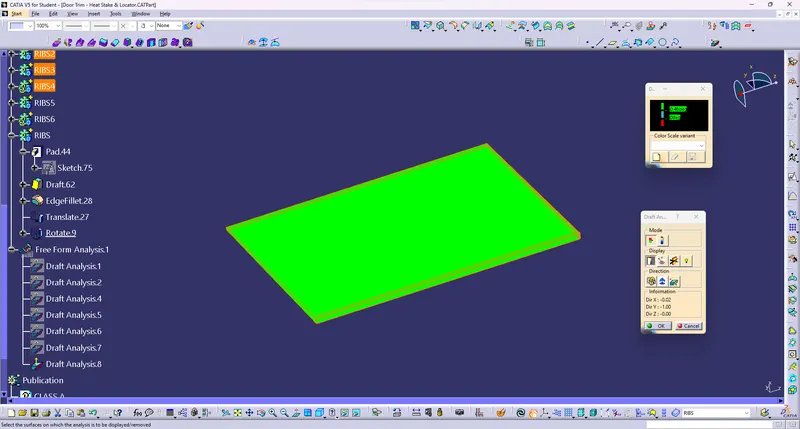
DRFAT ON HEAT STAKES
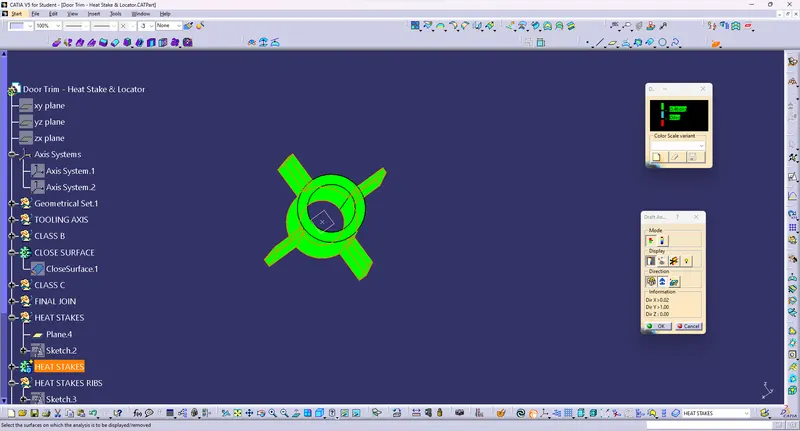
CLASS B SURFACE-
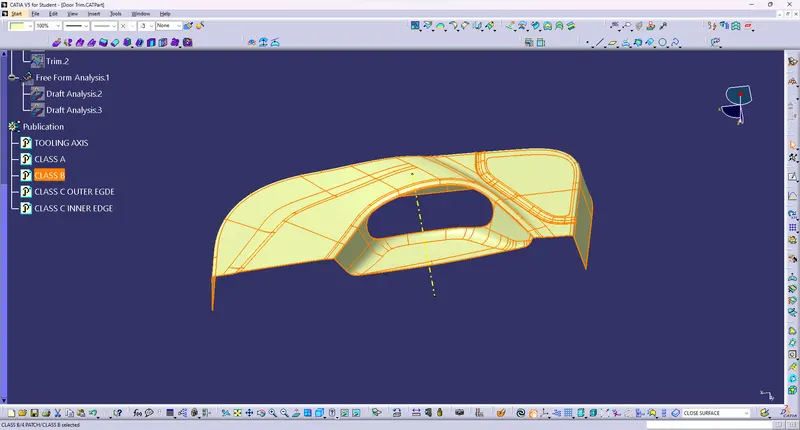
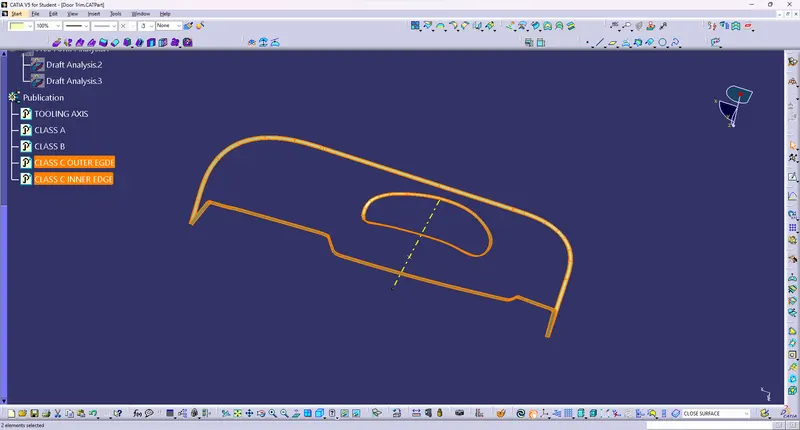
CLASS C-
CREATING THE RIB
Ribs are thin wall protrusions that extend perpendicularly from a wall or plane. They are usually found in clusters offering support to a plane that would have otherwise been too thick, but can also be stand-alone support for a single wall. They are commonly used to provide additional support and strength to a part. Thickness and location are essential to rib design.
First, the base surface where the rib has to be created is extracted using the Extract command.
Next, the profile is extruded, to find the height,h=Wall thickness * 5
=2.5*5
= 12.5 mm
Therefore, the height is 12.5 mm
The extruded surface is thickened,
Thickness,w=0.4*t
=0.4 2.5
=1mm
Therefore, the thickness of the rib is 1 mm
The draft is applied to the sides of the ribs. As per the design rule, the ideal draft angle is 0.5 deg
Then fillet is applied to the faces of the rib. As per the design rule, the fillet can be 0.25 mm.
Now, we have to check for the Rib root thickness.
To check for the Rib root thickness, We have to take an Intersection with the XY plane and the Coin holder component. Once we get to the intersection we have to create a tri-tangent circle at the rib area and measure it. The value must be within 30% greater of the wall thickness.
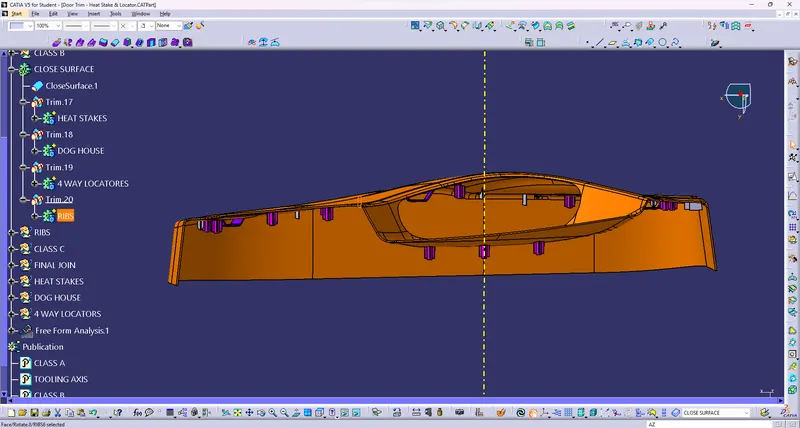
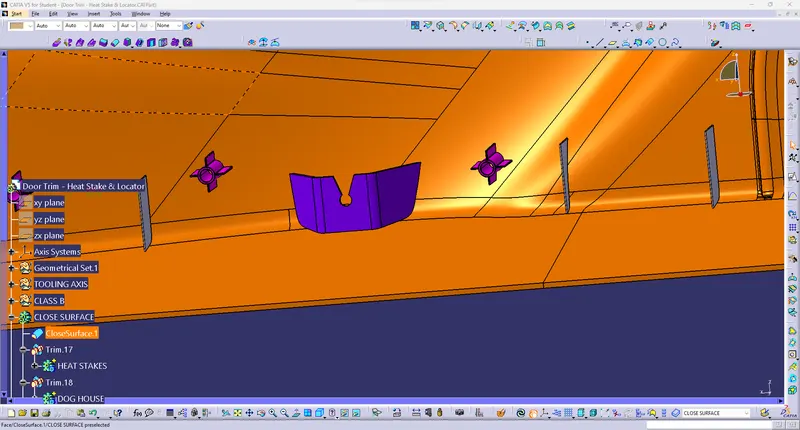
The locators restrict all the other degrees of freedom except the translation along the direction of tooling axis Le along y-axis. For restricting that degree of freedom we will be using the heat stakes.
In heat staking, we use local heating and cooling to raise the temperature of plastic components and allow plastic reforming to be carried out.
The draft is applied to the sides of the ribs. As per the design rule, the ideal draft angle is 0.5 deg
Then fillet is applied to the faces of the rib. As per the design rule, the fillet can be 0.25 mm.
The Orange colored cylinders are the heat stakes.
These heat stakes will enter the mating component and using a heat staking machine these heat stakes are melted and cooled. When cooled this will get hardened and the two components will stick together. Thus all degrees of freedom are arrested
Then, the ribs are created by following the rib design rules.
The draft is applied to the sides of the ribs. As per the design rule, the ideal draft angle is 0.5 deg
Hence, the ribs are created for the screw HEAT STAKES
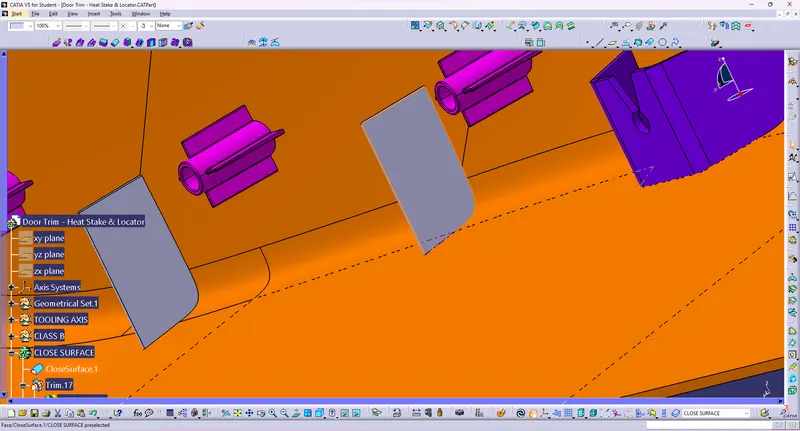
Now we will see how the plastic part is fixed onto the other plastic part. The door applique is fixed on to the door surface with the help of locators and heat stakes. Every component in space has 12 degrees of freedom. So these locators and heat stakes restrict all these degrees of freedom.
Locators are 4-way locators. The locators will follow the rib design guidelines and will be given a minimum draft of 0.5 degrees and a minimum fillet of 0.2mm and an entry chamfer of 3mm. This entry chamfer is given so that the locators can mate with the other part easily.
The draft is applied to the sides of the ribs. As per the design rule, the ideal draft angle is 0.5 deg
CREATING THE DOGHOUSE
The dog house is an engineering feature used in the plastic trim design. Dog houses are used as a supporting feature. Sometimes other engineering features like snaps; locators, etc. are mounded on them to increase their strength.
The doghouse is created by following the design rules.
The nominal wall thickness guide range is from 0.75 mm to 3 mm for reinforced materials and 0.5 mm to 5 mm for unreinforced materials.
Related Courses
WALL THICKNESS (W) = 0.70 (NOMINAL THICKNESS OF PLASTIC MATERIAL)
This process is usually done by Thicken surface command.
The fillets and the draft are given as per the design rules.
An important thing while designing a doghouse is to maintain 40% less thickness than the wall thickness (T) at the area of the intersection to avoid sink marks. So, a C shape is formed at the intersection.
This can be made using the split command to remove the solid at the intersection
ISO VIEW
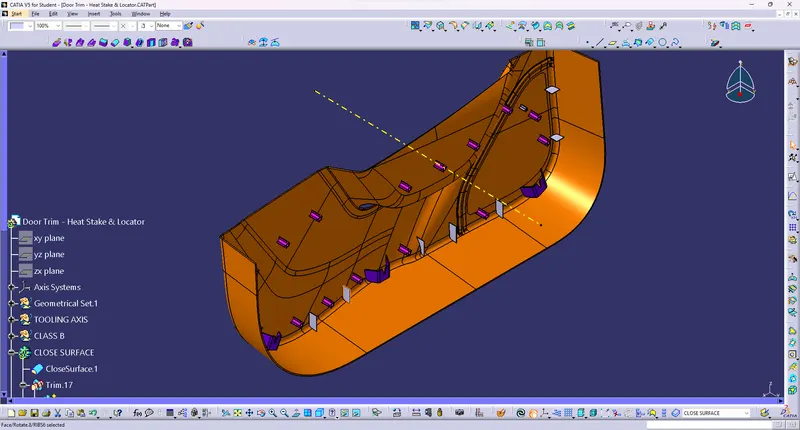
SIDE VIEW
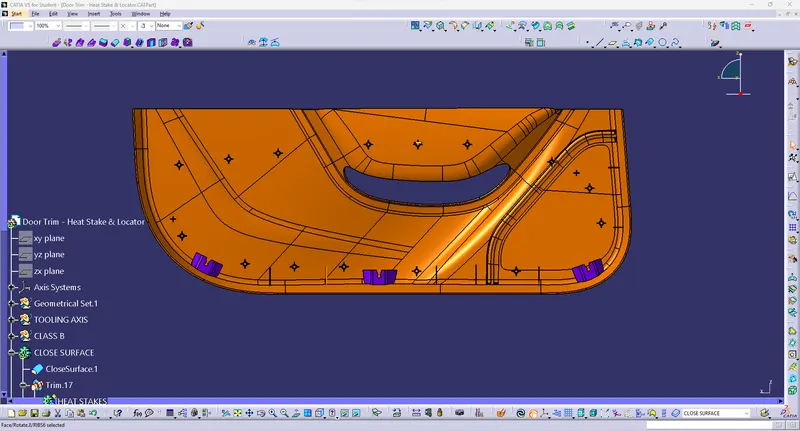
FRONT VIEW
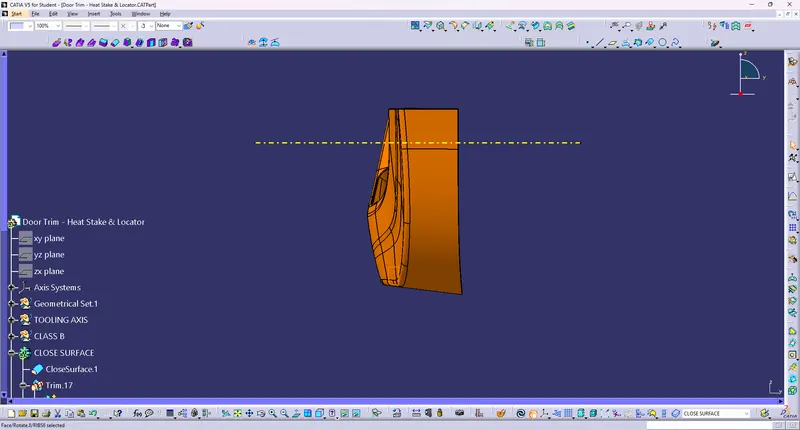
TOP VIEW