Week 9 - Project 1 - Door Trim Lower with Engineering Features
AIM : To create the Door Trim Lower Design Plastic component through the given Class-A surface. Also create the engineeing features as 4way locaters and heat stakes.
Objective
- To create a tooling direction.
- To perform draft analysis for given A-Surface and prepare the final close body.
- To design the Bumper plastic component by creating the B-Surface and C-Surface using the given Class-A surface.
- Take the Thickness of the component to be 2.5 mm.
Introduction :
The input of the product designer is in the form of the A-class surface. The job of the product designer is to create the B and C surfaces keeping all the aspects for the mold.
Class A Surface is
- Visible surface and aesthetic look.
- Surface with textures.
- Surfaces provided by customer(OEM).
- Don't have any features like(rib, snap, bosses, etc) on class A surface.
- Class A surface is made from scanned data with different software like alias etc.
- Surfaces which are having CURVATURE CONTINUITY IS CALLED class-A.
Class B surface is
- Invisible Surfaces.
- Surface mostly don't have textures.
- Surface needs to be created according to the class-A surface.
- Having all features(Rib,boss,snap etc) in B-side surface only.
- Surfaces which is having TANGENT CONTINUITY IS CALLED class-B.
Class A Surface : Check the connectivity of the Class A Surface Ensure that there is no gap between the component, using join command. We can visually check it or by clicking boundary command. It has a boundaries outer. Therefore first check completed.
Below fig 1 shown the given A-class surface.
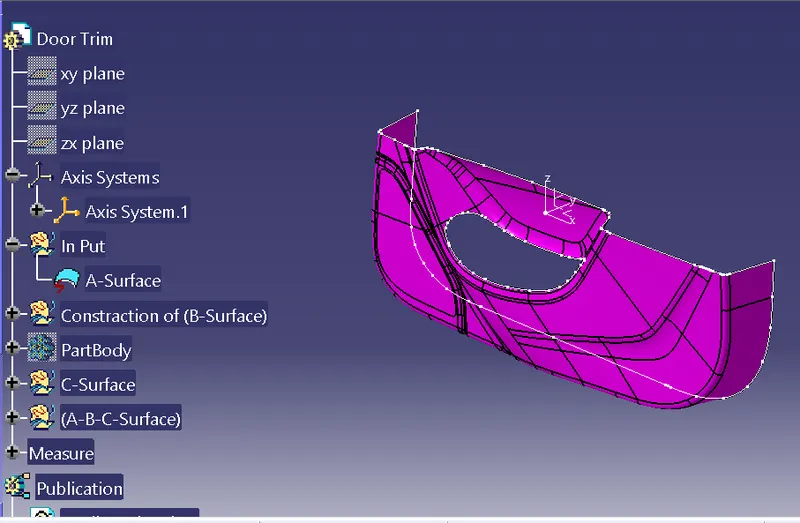
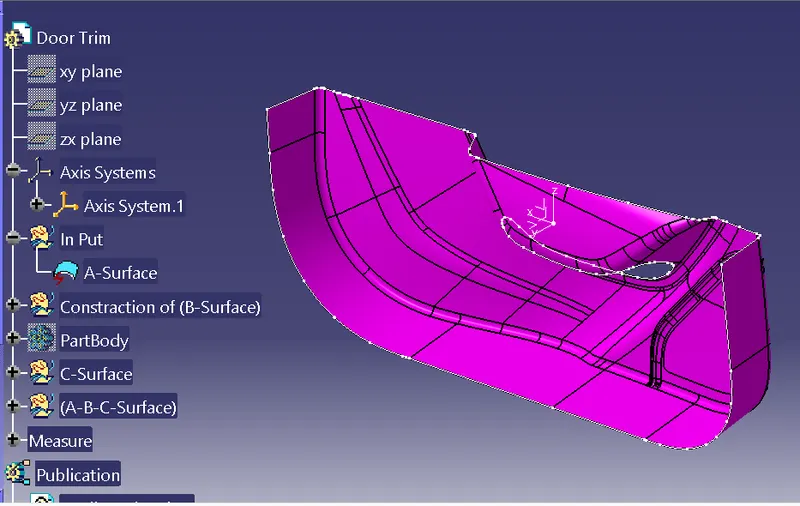
Fig 1.
The given A-Surface having No gap as above fig shown. Hence boundary generated at the edges.
Procedure :
Tooling Direction for Plastic Part : Tooling direction is main consideration for plastic part and mold parts because it defines movement of mold part and possibility of plastic part to come-out from mold part (Core and Cavity).
- In Molding machine arrangement is given to open the mold along a direction which is known as Tooling Direction.
- In other words. The mold is built from two separate halves (Core and Cavity) and tooling direction basically define the direction of mold pulls apart.
- Tooling direction is known as primary direction.
- One more new metohd to find the tooling direction is by using the CG(Centre of gravity) part and crete line centre point and one flat surface.
Preparation of Tooling Direction
While creating the tooling direction in given class A surface. Chose the one suitable Base and Side wall and draw the line direction of axis. as shown the below fig 1.1.
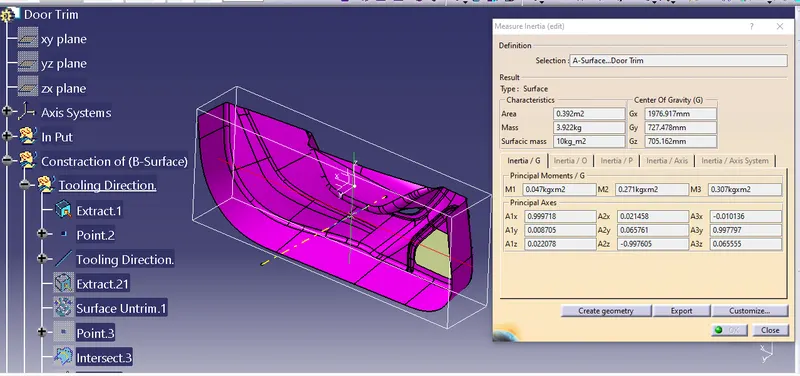
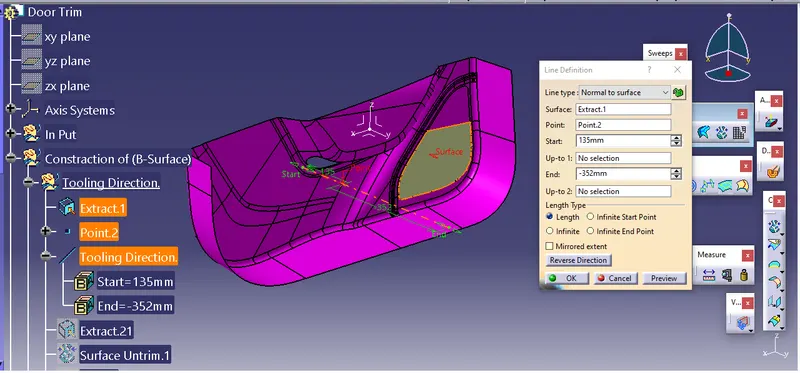
Fig 1.1.
While preparing the tooling direction i followed method is chose the Centre of Gravity. Which is help us to find the centre point, there draw the line with the help of point and one flat surface. Hence we consider the final tooling direction.
Below fig 1.2 shown the A-Surface Draft analysis.
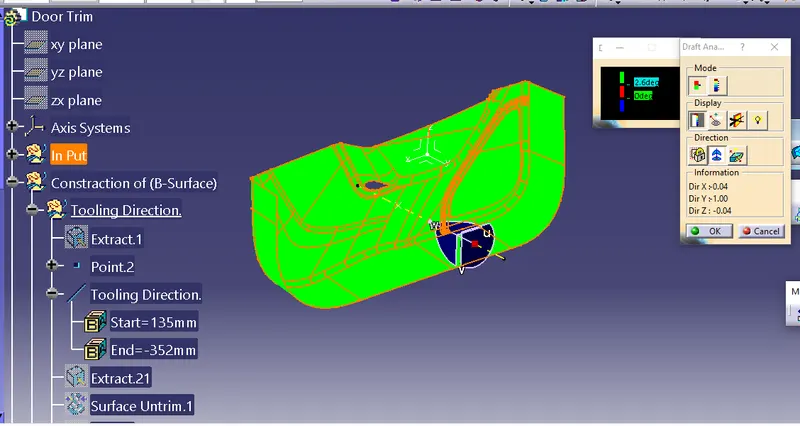
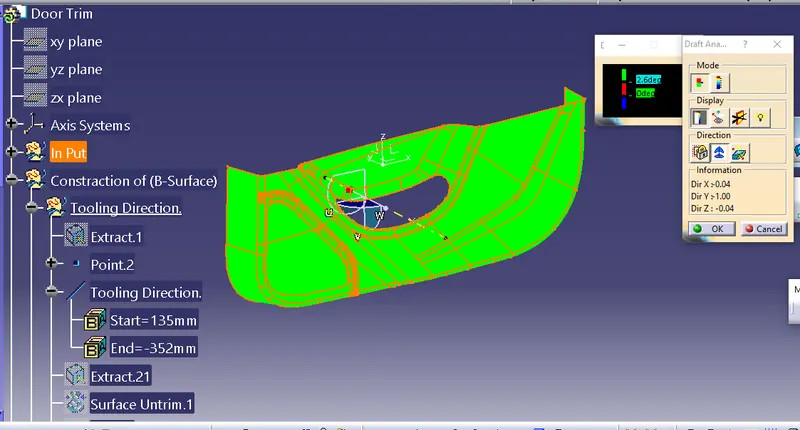
Fig 1.2.
Creation of B-Surface: Is created with help of A-Surface by using the Off-set,Trim command,Multi Section,Sweep and Fill command. Below fig 1.3 shown B-Surface.
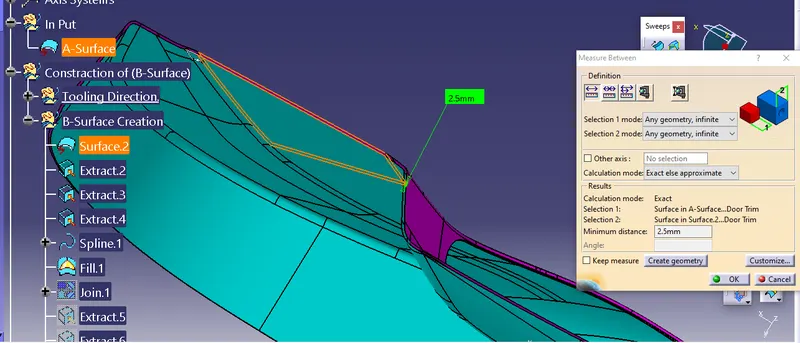
First offset the class surface with 2.5mm as per requried thickness.
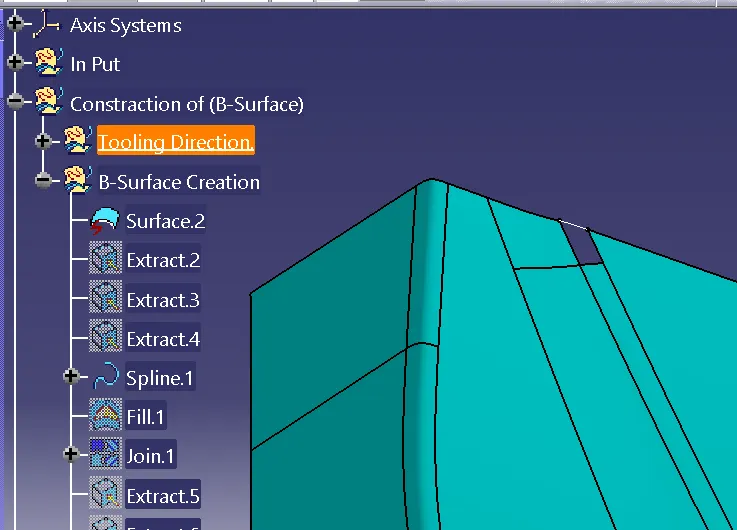
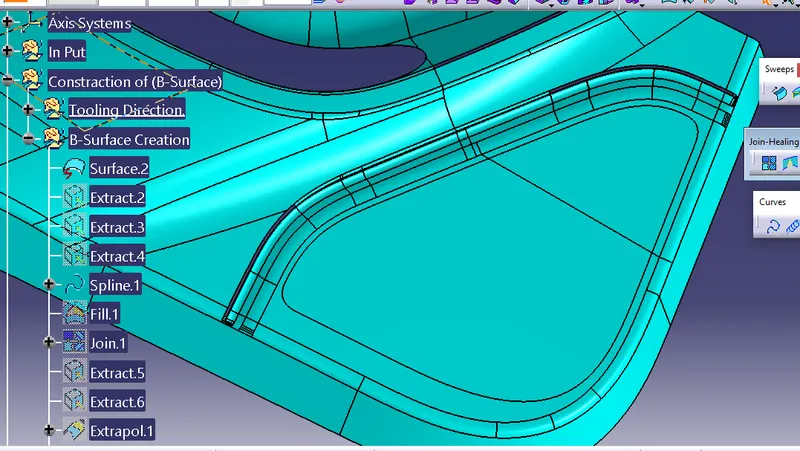
In offset surface having on some patches are removed. For this patches we need create the close surface while using commands.
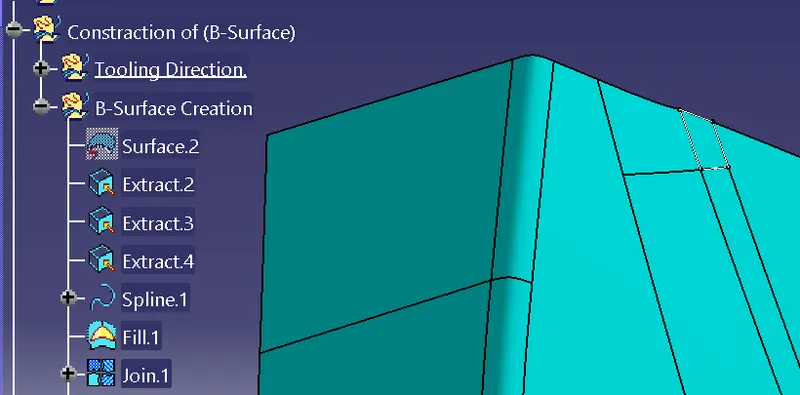
Gap is filled with fill command.
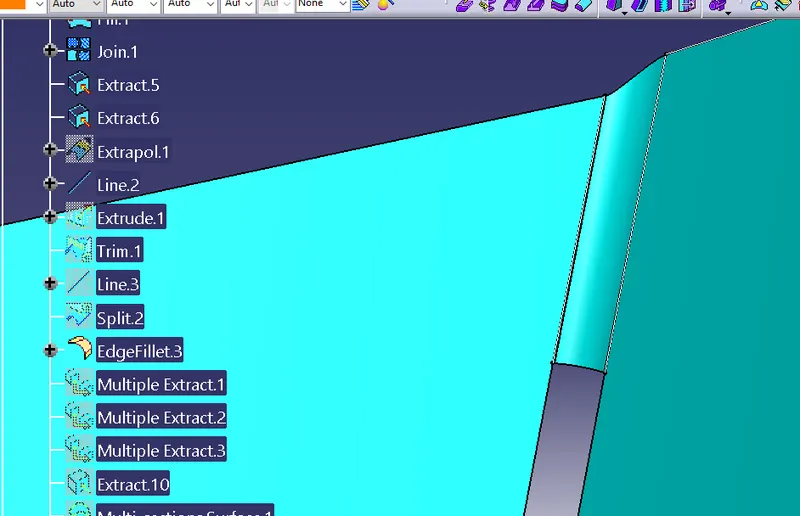
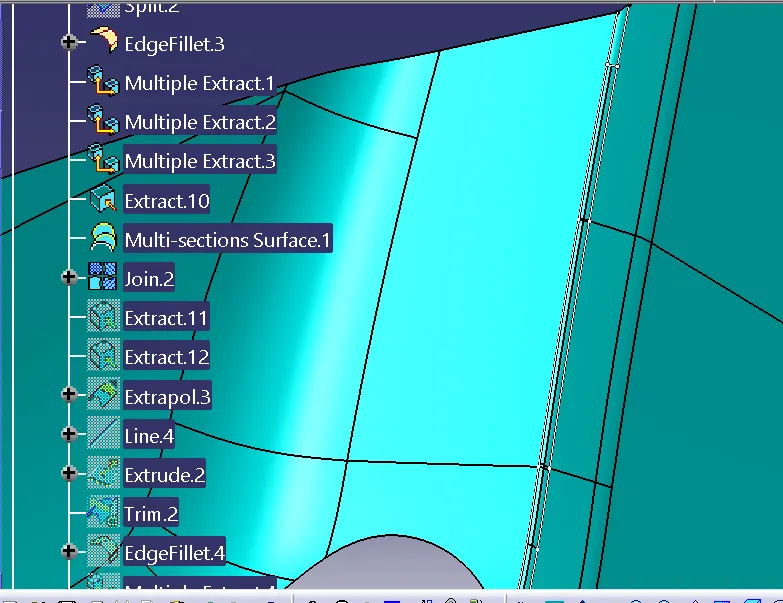
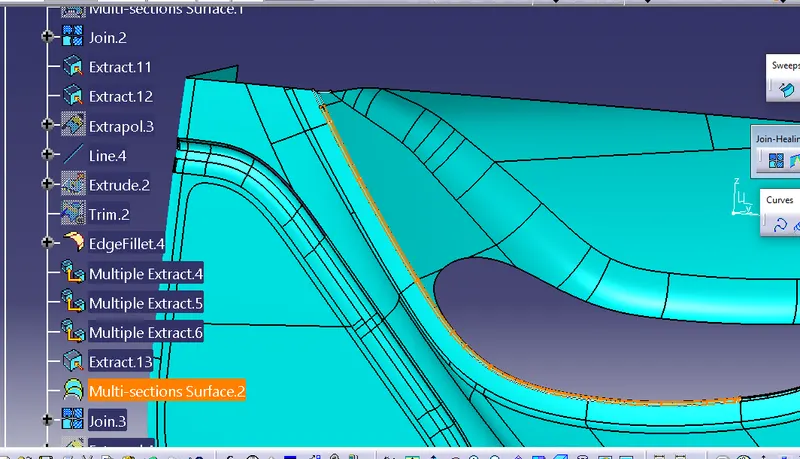
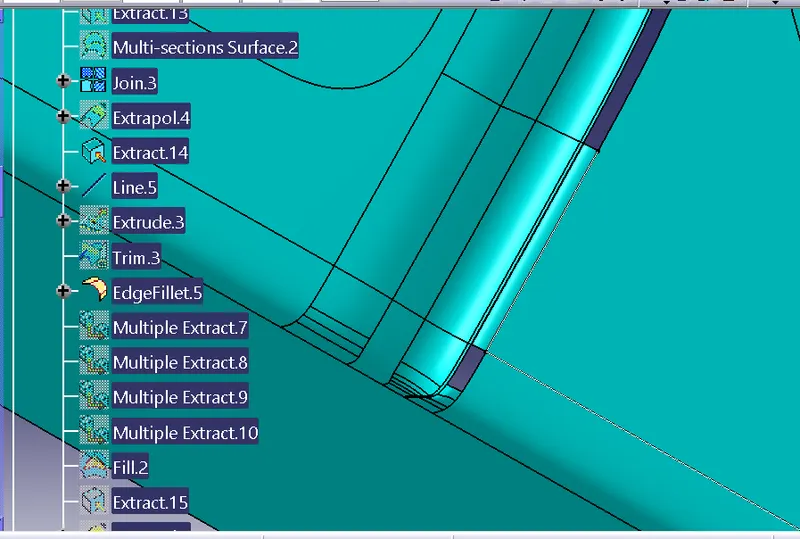
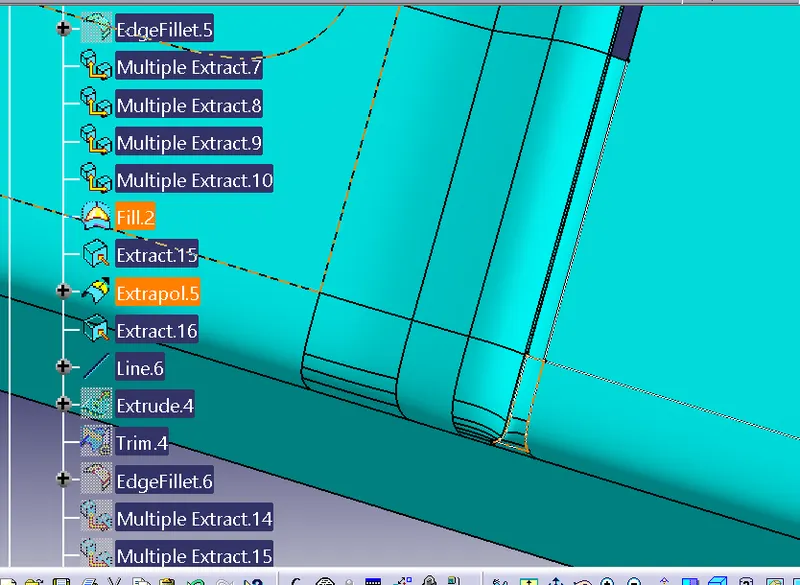
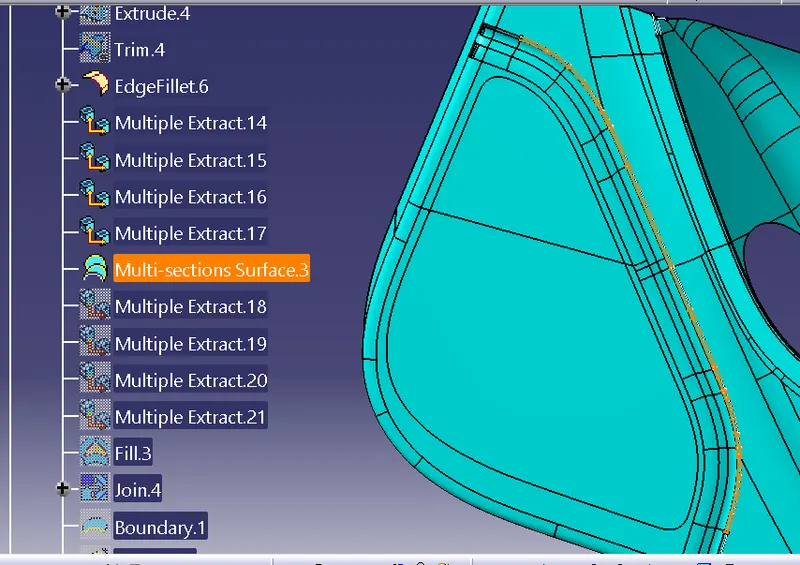
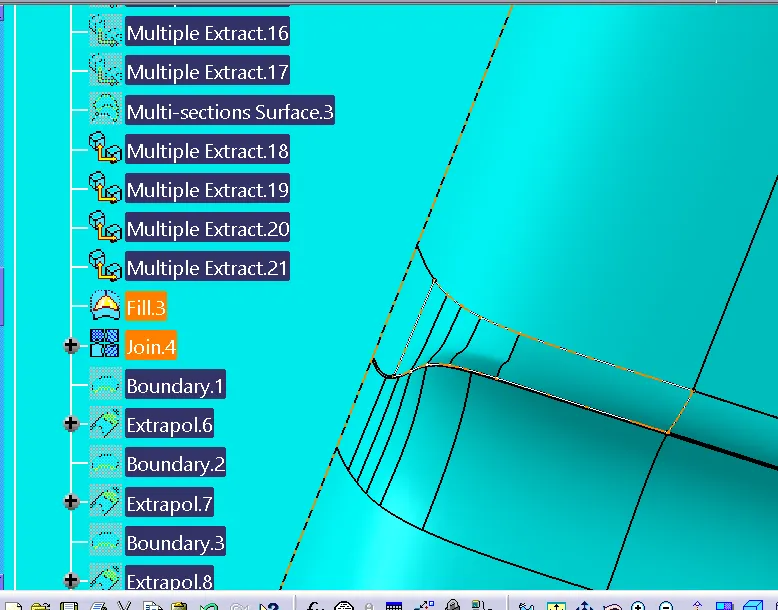
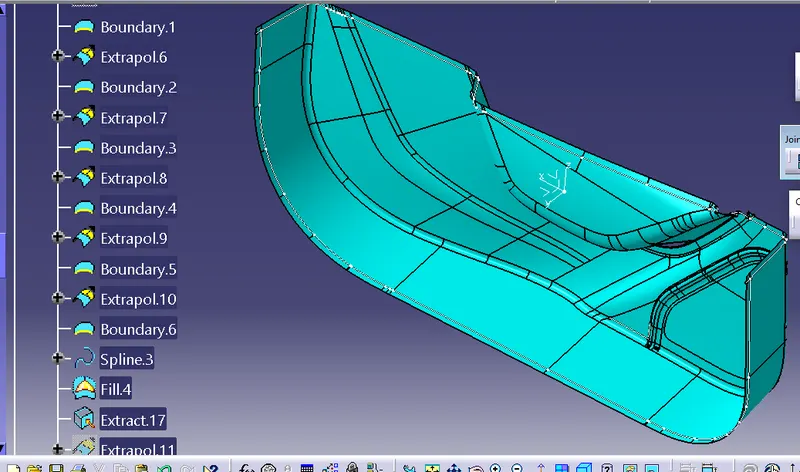
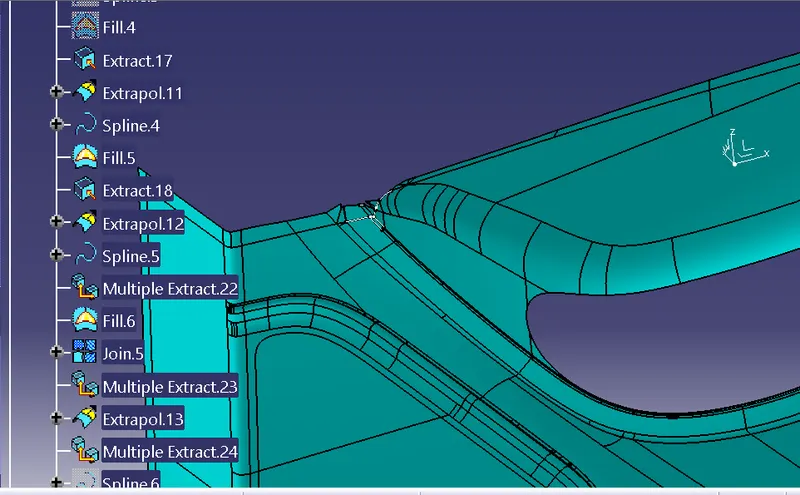
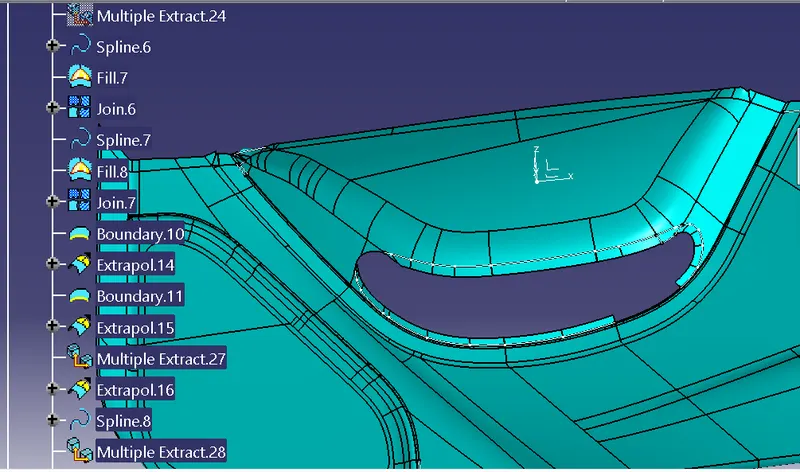
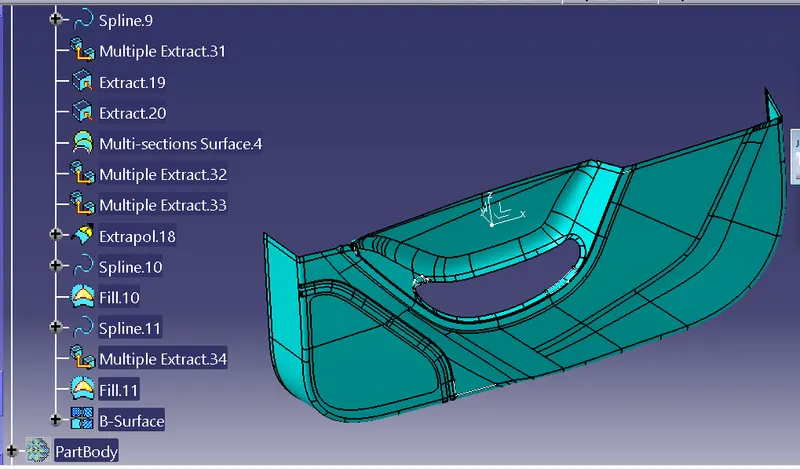
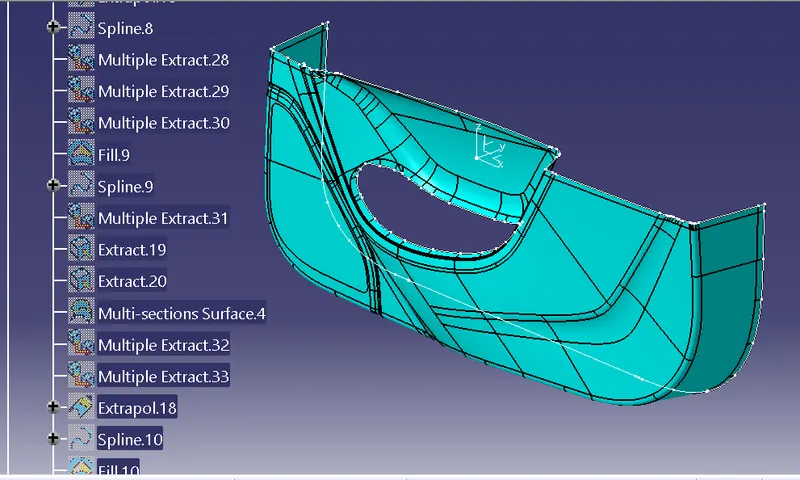
fig 1.3.
The above fig 1.3. boundary line are created at edges. Hence surface is closed.
Creation of C-Surface: Is created with help of A-Surface by using the Sweep and Boundary command. Below fig 1.4 shown C-Surface.
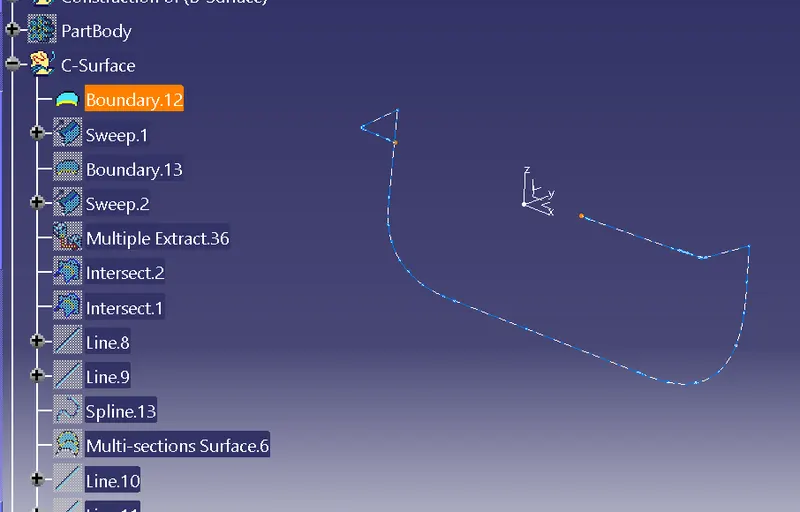
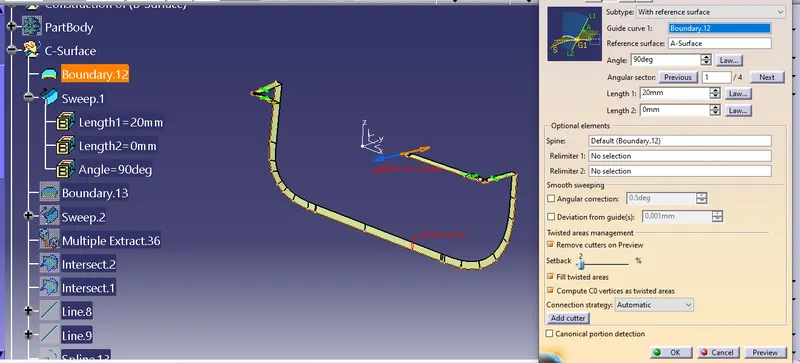
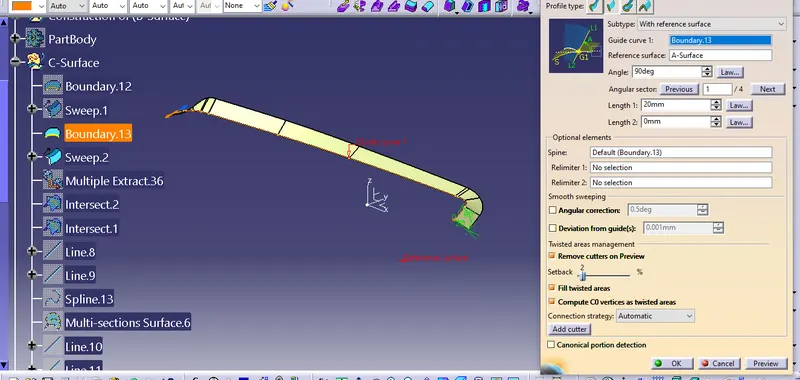
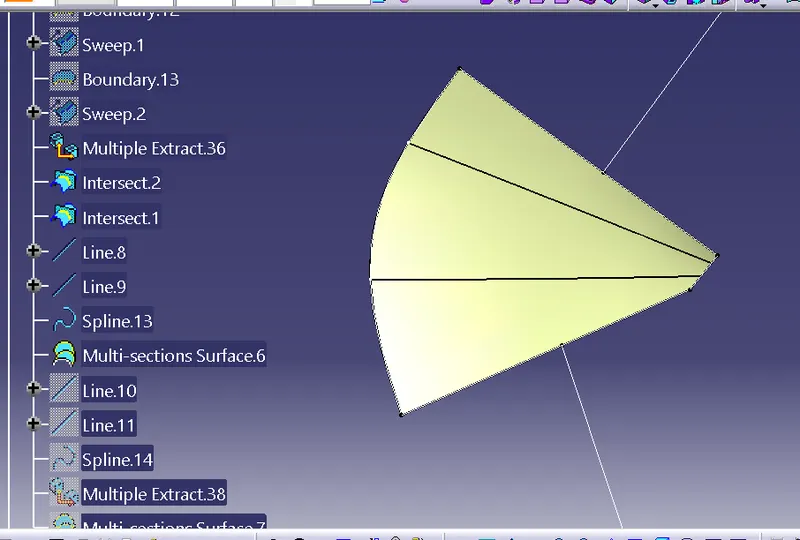
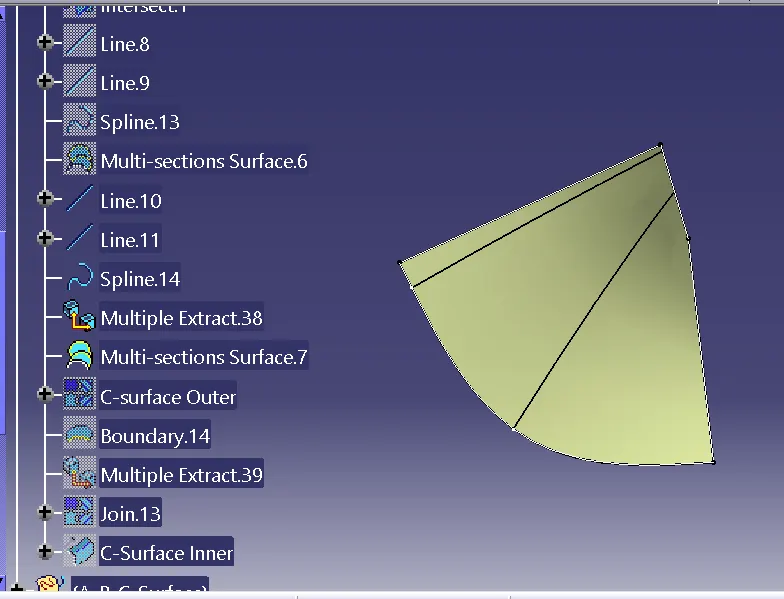
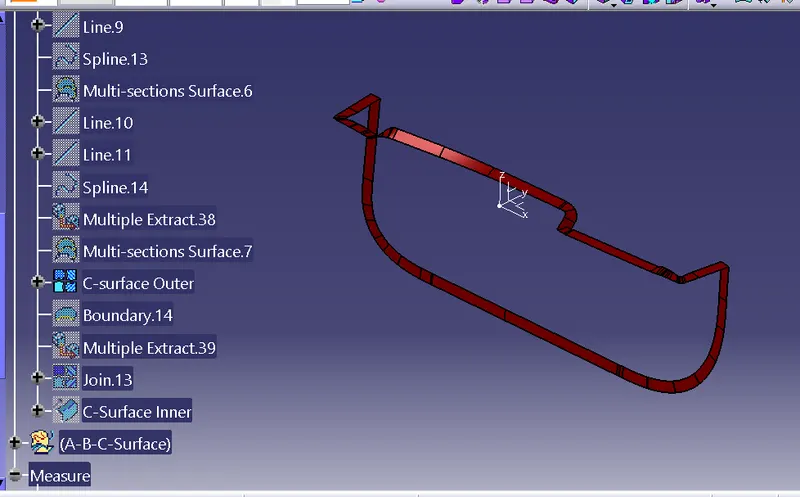
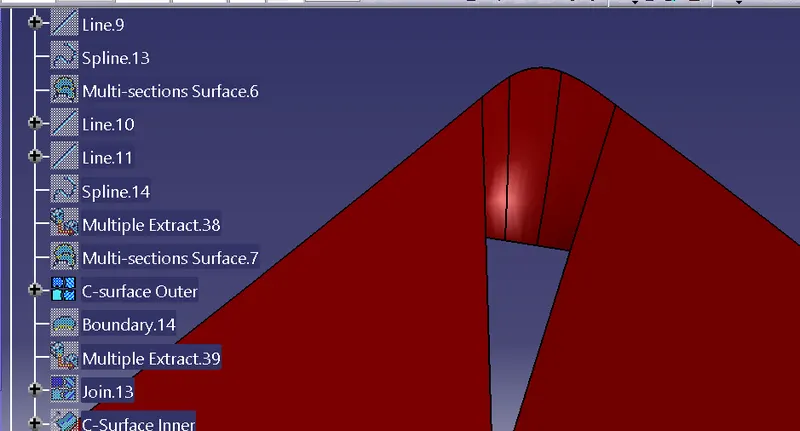
In radius area there will be little bit complicated in such case by using the Multi Section Method to create surface.
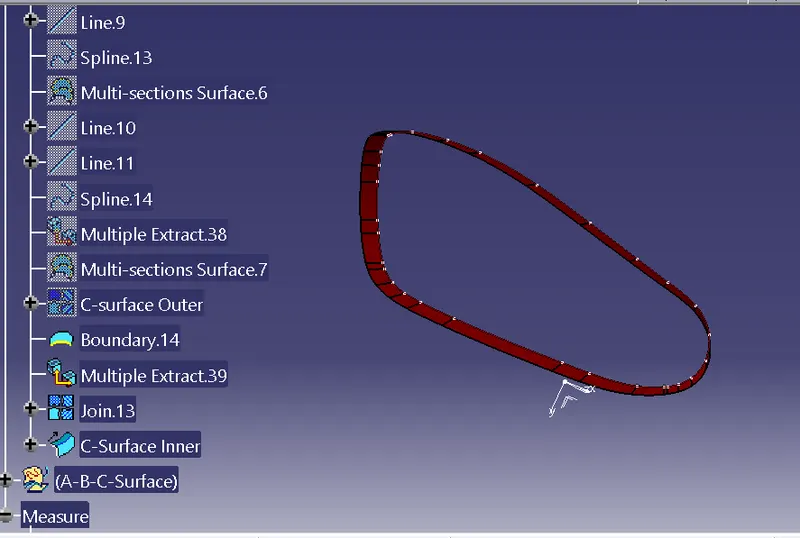
fig 1.4
Below fig 1.5 shown the joing of A-B-C-Surface with Draft analysis checking.
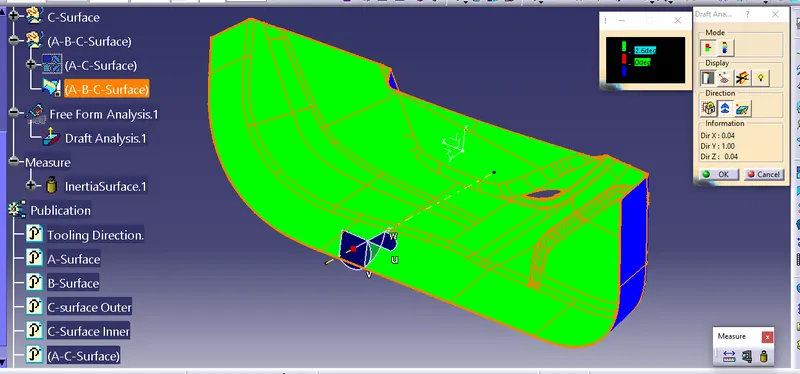
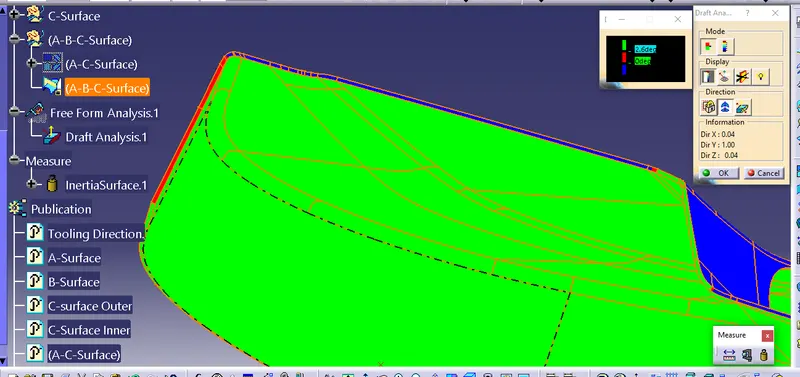
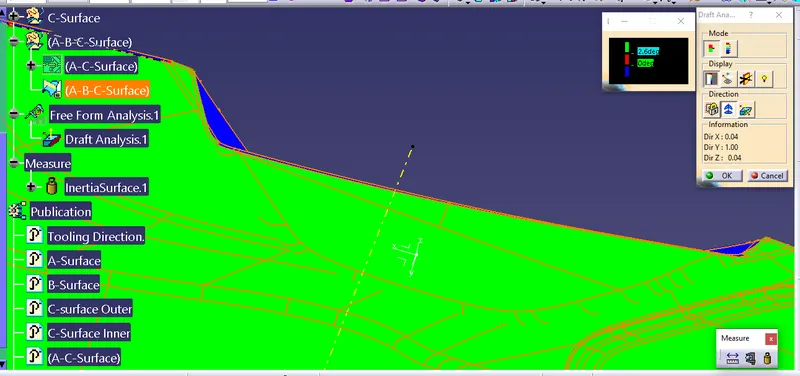
Fig1.5.
In C-Surface having an Negtive Draft need to check with A-Surface.
Below Fig 1.6 shown the Close Surface and some Publication.
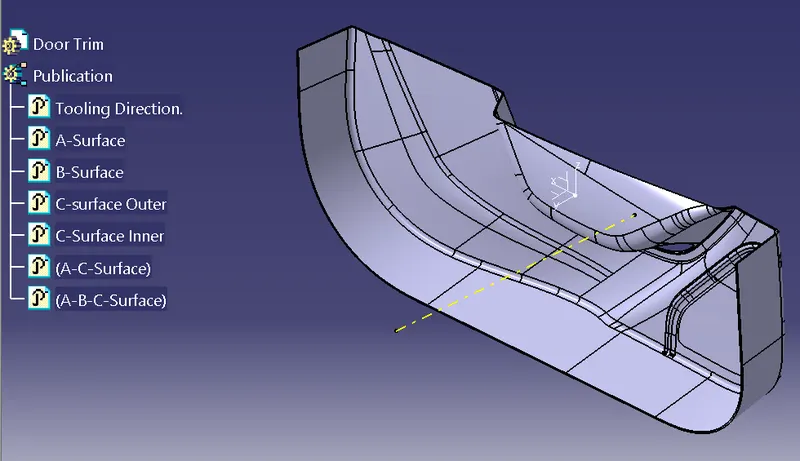
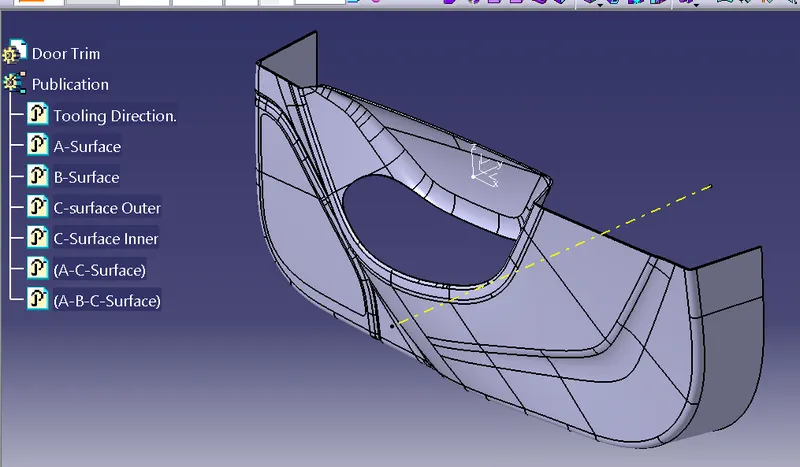
Fig 1.6.
B Side Features:
1.7 Heat Stake Design:
Heat Stakes are designed as per the design considerations as Below fig shown.
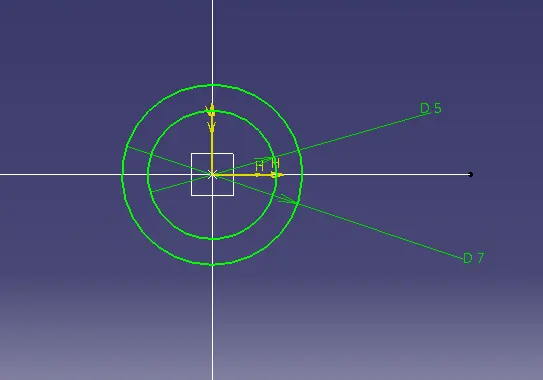
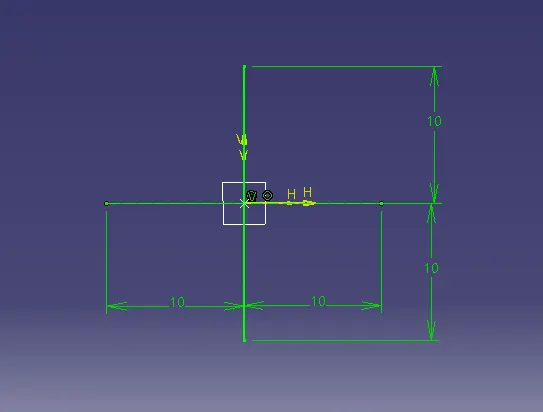
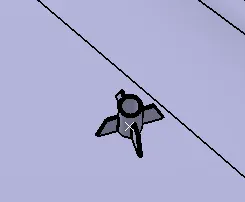
Fig 1.7 Heat Stakes.
Main use of heat stake is welding between the two parts like remolding it will help to joining the 2 parts.
The heat stake is designed with a sketch and is initially assembled inside a Body called Heat Stake Assembly and then the feature is combined with the part body using Boolean Operation.
1.8 Locator Design:
Locators are designed as per the design considerations and located at the points there will be control the degree of freedom. Below fig shown.
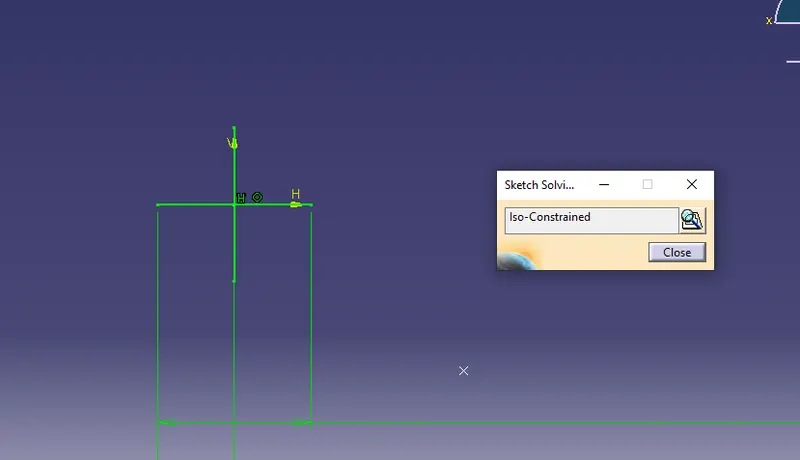
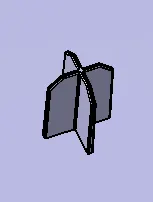
Fig 1.8 4way locater.
Main purpose of lacater is to guide the direction and control the position between 2 mating parts. as above fig shown.
1.9 Checking the draft analysis of B-Side features.
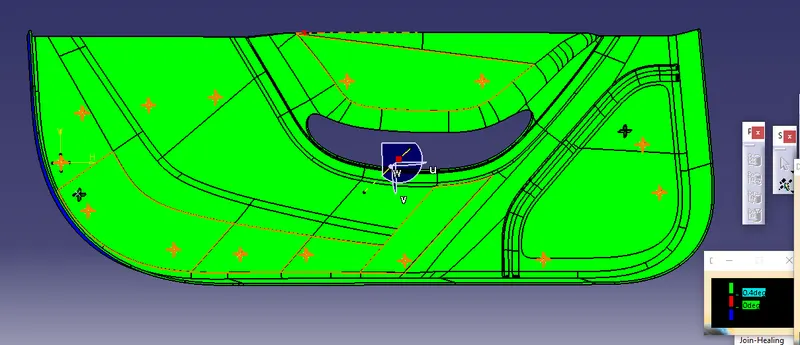
Fig 1.9 Draft analysis.
Below fig (1.10 to 1.13) shown solid model with the proper color code of the draft angle in various orientations (Isometric, Front, Side, and Top View).
Isometric View.
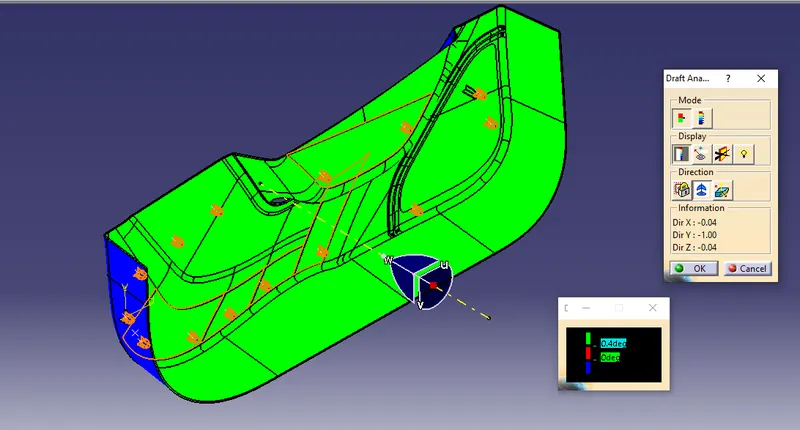
Fig 1.10.
Front View.
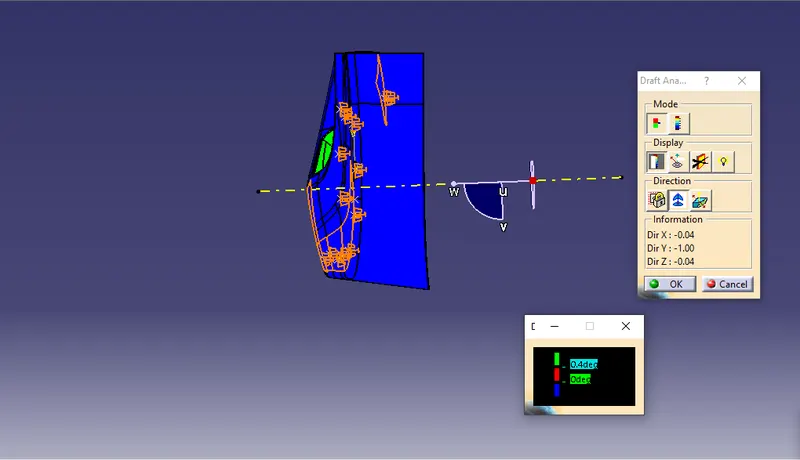
Fig 1.11.
Side View.
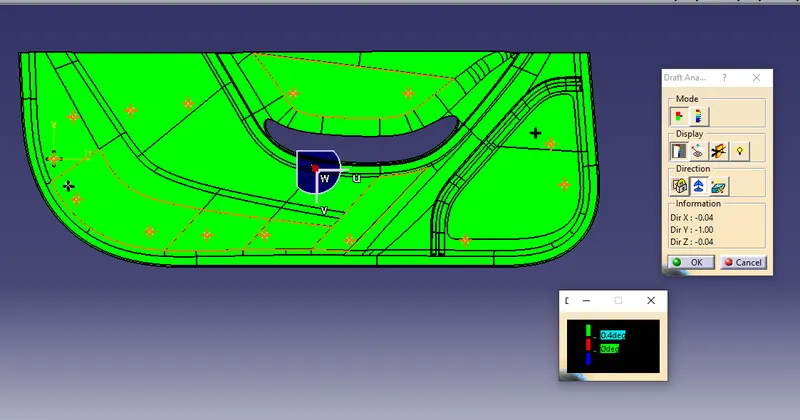
Fig 1.12.
Top View.
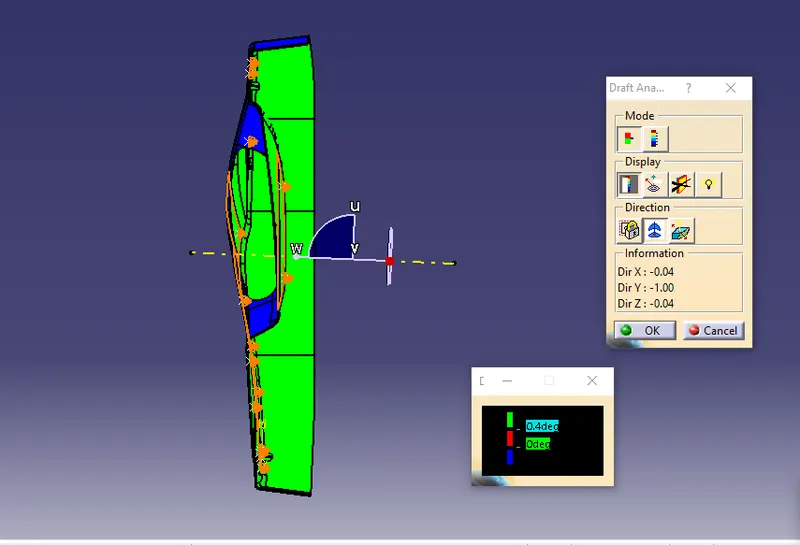
Fig 1.13.
Note : In C-Surface having an Negtive Draft need check with A-Surface.
Conclusion : The Door Trim Lowe is created with consedering all Design Methodology and also created the engineering features.