Week 9 - Parametric study on Gate valve.
Aim:
To perform a parametric study on a gate valve at different valve opening settings.
Theory:
Gate valves work by inserting a rectangular gate or wedge into the path of a flowing fluid. They are operated by a threaded stem which connects the actuator (generally a hand wheel or motor) to the stem of the gate. If the valve has a rising stem its position can be seen just by looking at the position of the stem. A gate valve is used to control the fluid flow through lifting and descending the gate. A gate distinct feature is to provide an unobstructed passageway, which includes minimal pressure loss over the valve.
When the gate is fully opened there is no restriction to the flow hence the pressure drop is low comparatively. Generally, the gate valve are fully closed or fully open as partially opened valve may experience vibration which may lead to excessive wear. A gate valve's main component is body, seat, gate, stem, bonnet, and actuator. the primary mechanism is straight forward where the handwheel is rotated to move the gate up and down via threads. they require more than a 360-degree turn to fully open the valve.
Gate valves tend to be slightly cheaper than ball valves of the same size and quality. They are slower in actuation than quarter-turn valves and are for applications where valve operation is infrequent, such as isolating valves. Gate valves should be used either fully open or fully closed, not to regulate flow. Automated gate valves exist with either an electric or pneumatic actuator, but a manual gate valve is cost-effective since they have infrequent usage. Gate valves are widely used for all types of applications and are suitable for both above-ground and underground installation. They are suitable for most fluids including steam, water, oil, and gas, etc.
Part-1:
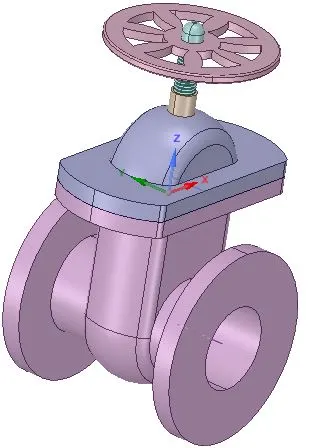
The solid geometry consists of bottom housing, handwheel, spindle, bonnet, and gate valve. The fluid moves from the inlet to the outlet, the gate valve is used to restrict this motion, and this is actuated manually by turning the handwheel which is supported by the bonnet and is connected via the spindle. When a lesser mass flow is required at the outlet, the gate valve is lowered, which restrict the mass flow of the fluid at the outlet. The mass flow rate of the fluid at the outlet varies with the lift of the gate valve stopper, and that is to be simulated.
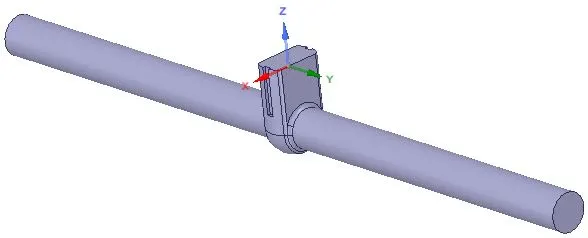
To simulate the effect of the stopper on the mass flow rate of the fluid at the outlet the stopper is moved 10mm in the positive Z-direction so that the flow path is partially open. This is parametrized. Next, the fluid is extracted from the solid geometry. The parameterization helps us change its value and compute the required output parameters without having to repeat the same processes again. Since we are not interested in the analysis of solid geometry, it is suppressed.
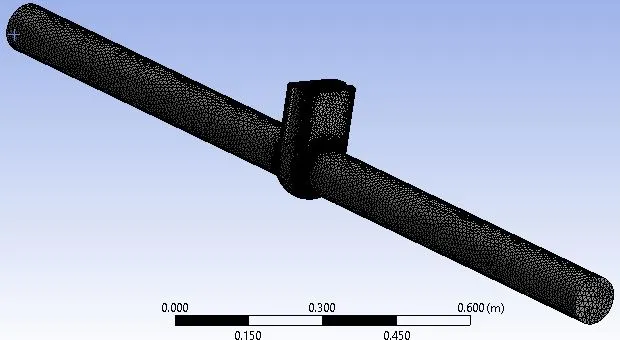
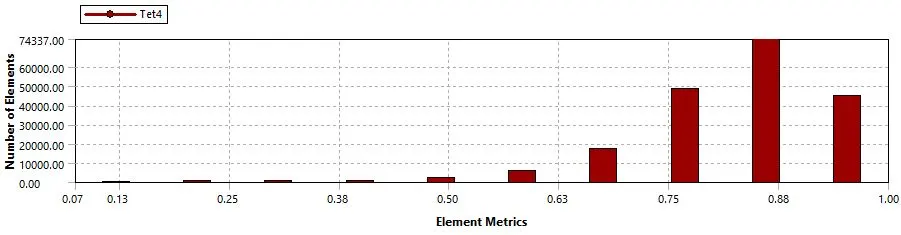
Once the geometry is defined, the meshing is done. The mesh element size taken was 10mm. Once the required mesh was generated, a total of 40524 nodes and 193912 elements were generated.
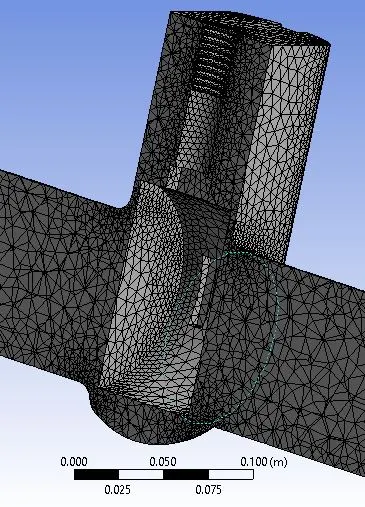
The resultant mesh quality is as follows
The fluid medium is water. Acceleration due to gravity is taken into consideration (along the negative Z-direction). The problem was solved using the steady-state equations, and the K-epsilon realizable turbulence model with scalable wall functions was used.
The boundary conditions at the inlet and outlet were pressure inlet and pressure outlet. The gauge pressure at the inlet and outlet is 10 Pascals and 0 Pascals respectively. When standard initialization was done from the inlet, the velocity computed was 0.1415488 m/s.
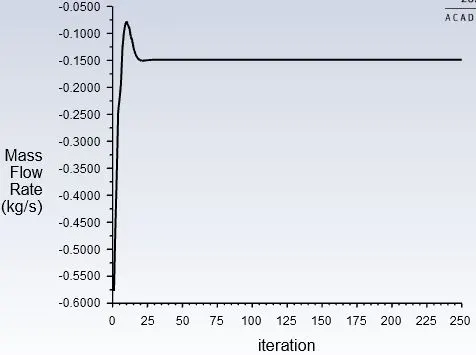
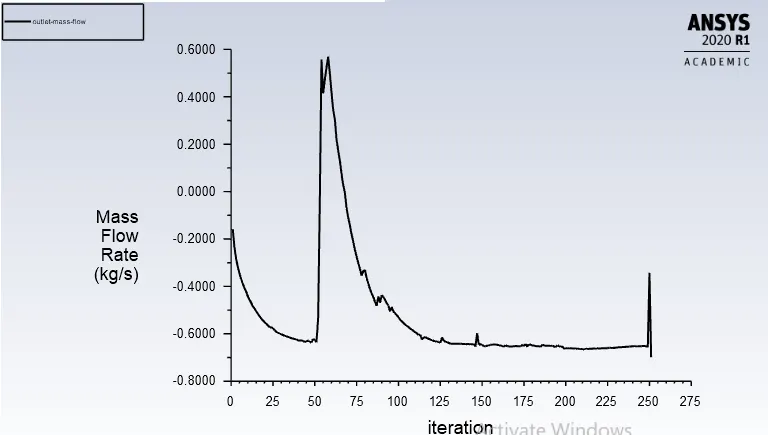
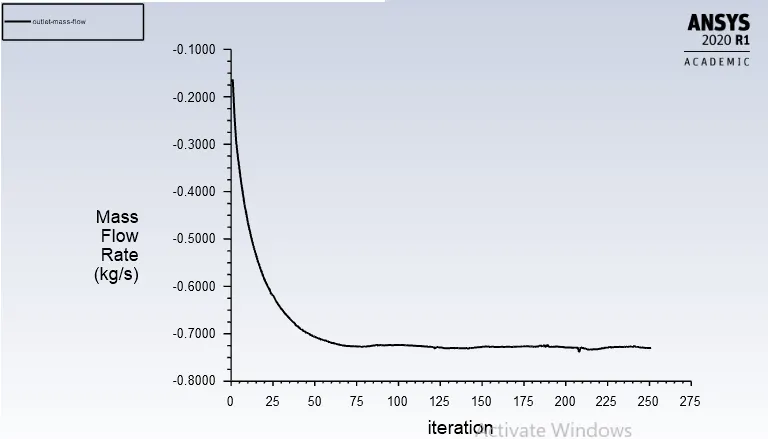
A flux report of mass flow rate is created and it is defined as an output parameter so as to calculate this property at different positions of the stopper. The plot below gives the mass flow rate of the fluid at the outlet at 10mm lift of the stopper.
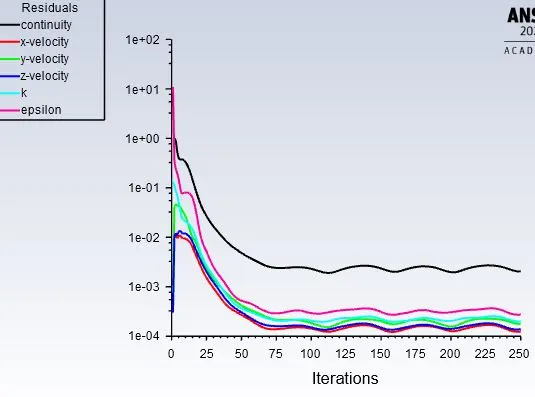
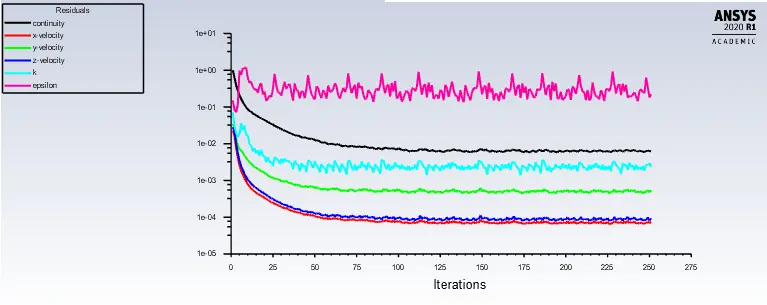
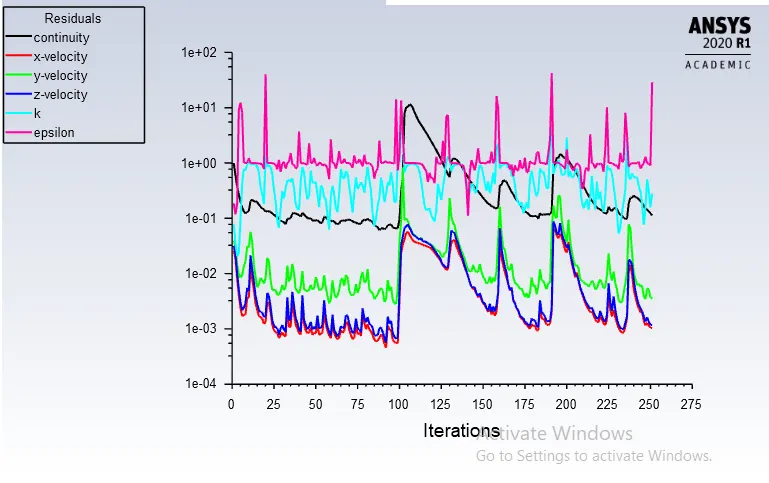
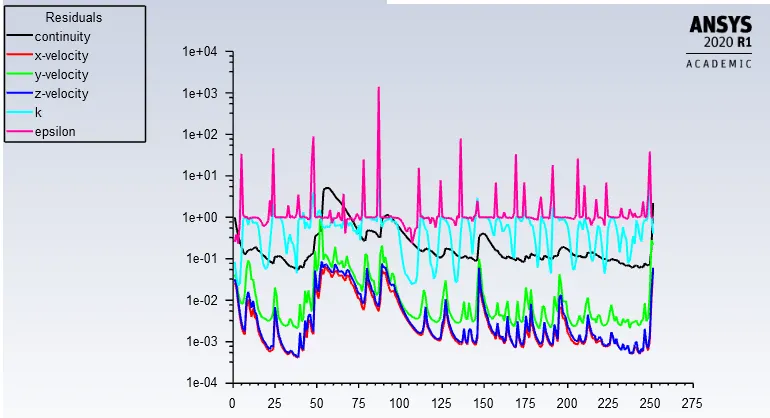
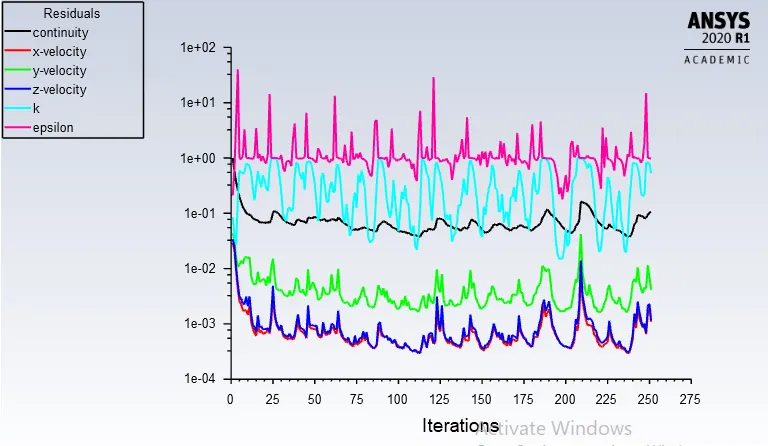
The solution was run for 250 iterations. and the residual plot is as follows
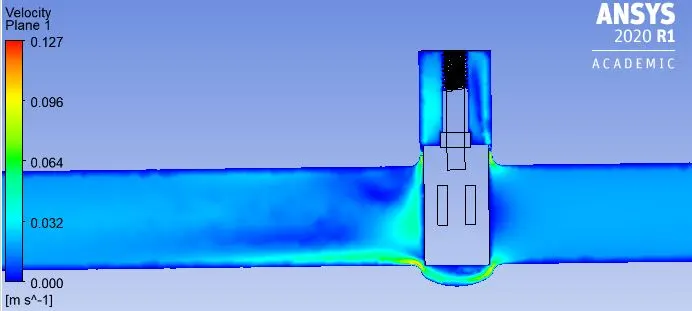
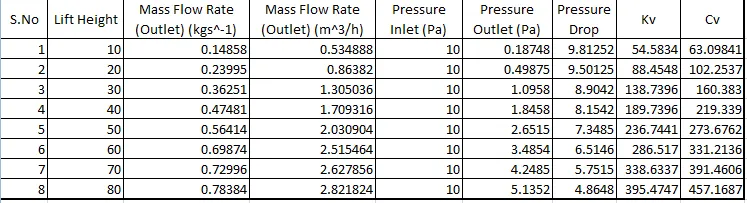
Next, we move on to the parameters tab to calculate the mass flow rates for the different stopper heights, and the following results were obtained
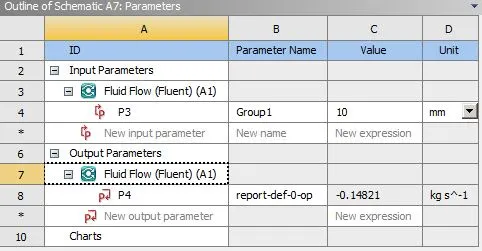
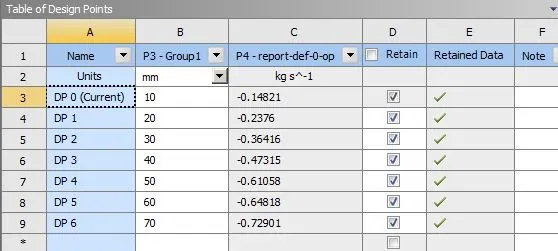
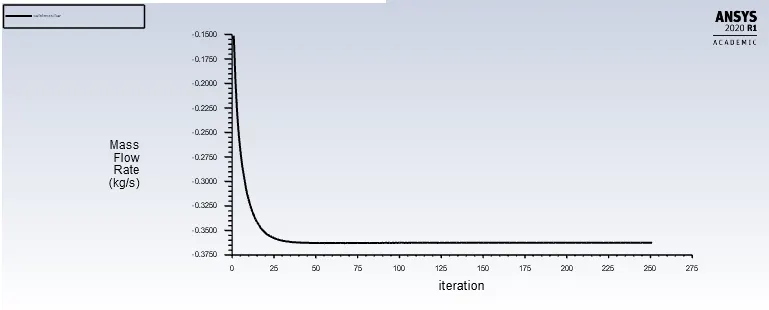
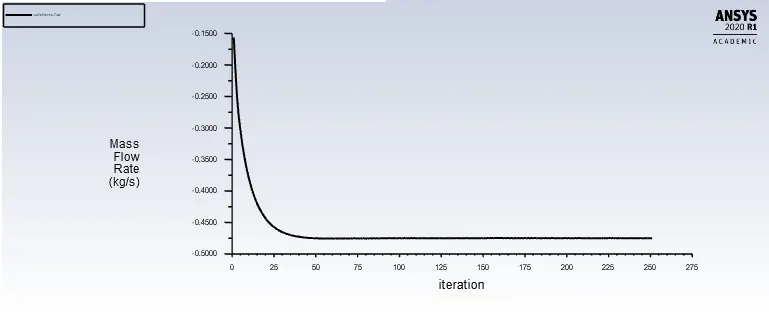
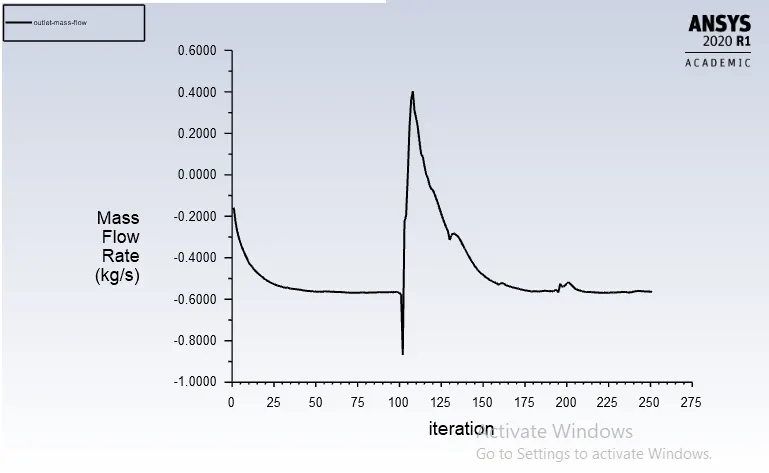
The negative signs for the mass flow rates imply that the fluid is exiting the domain. The mass flow rate is calculated for the stopper lifts from 10mm to 70mm. The mass flow rate increases with the increase in the lit of the stopper. When the stopper is lifted gradually, the space available for the passage of the fluid increases hence the mass flow increases. When we perform the parametric study, Ansys automatically changes the mesh as per new geometry using the same mesh specifications given earlier, and solves and calculates the output parameters, thereby saving time comparatively if it was done manually.
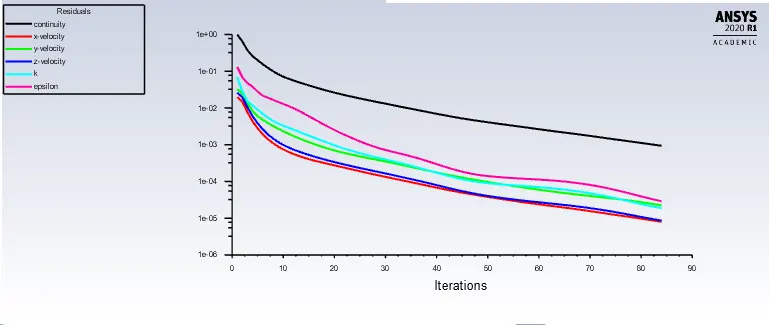
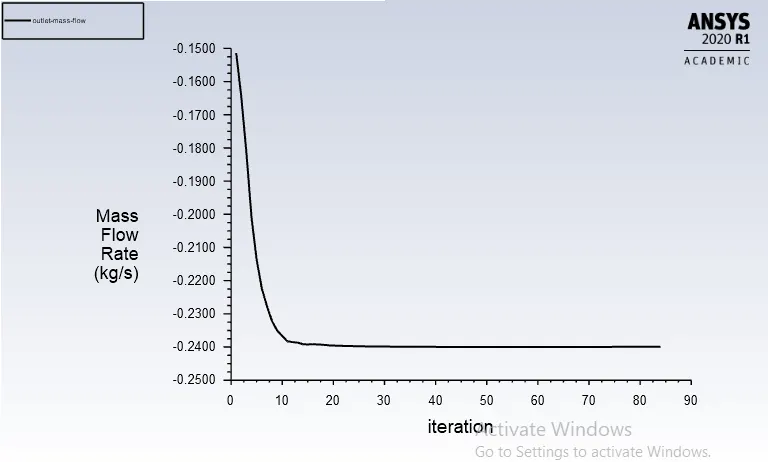
The results for the gate disc with 20mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
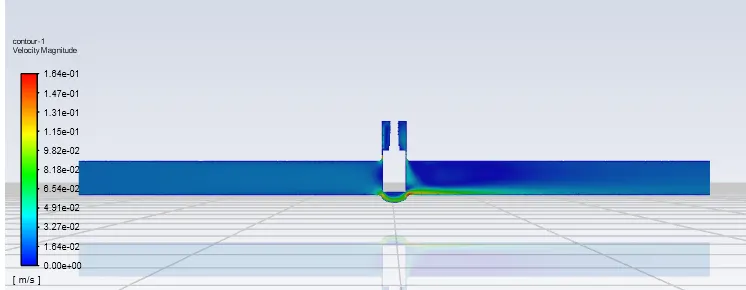
3. Velocity Contour
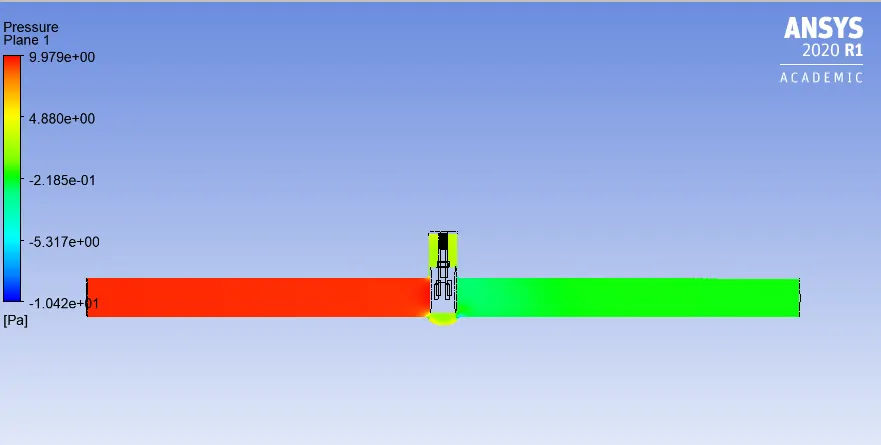
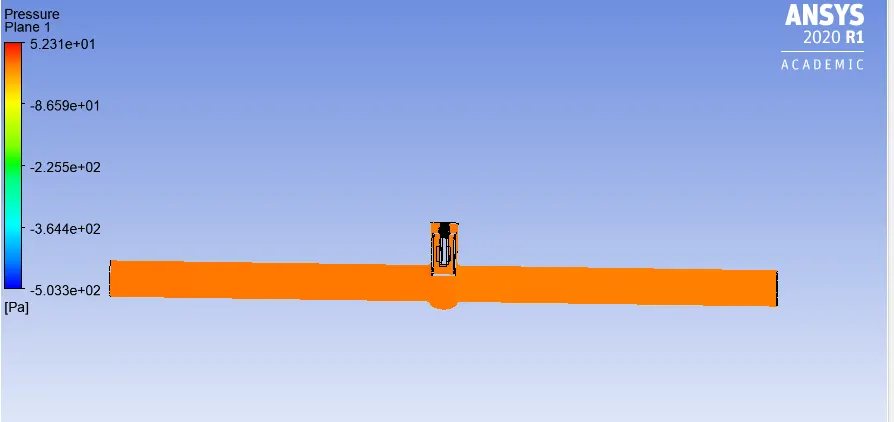
4. Pressure Contour
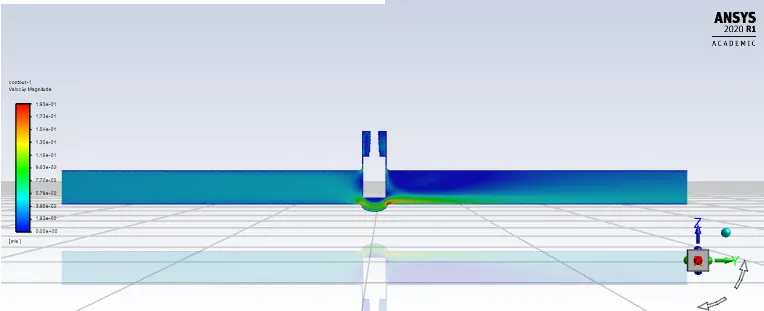
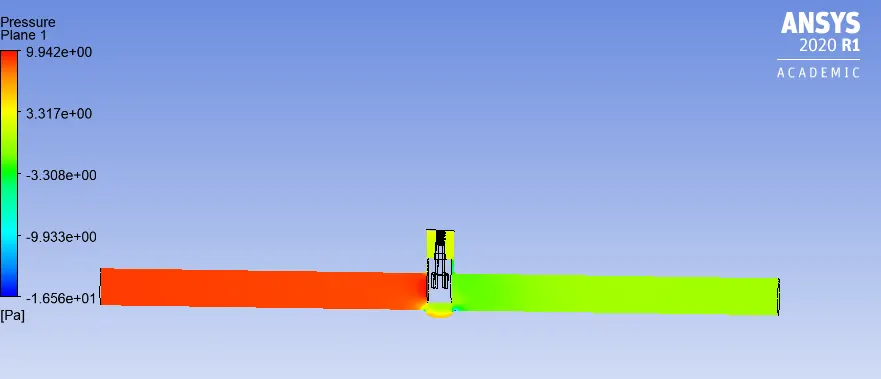
The results for the gate disc with 30mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
3. Velocity Contour
4. Pressure Contour
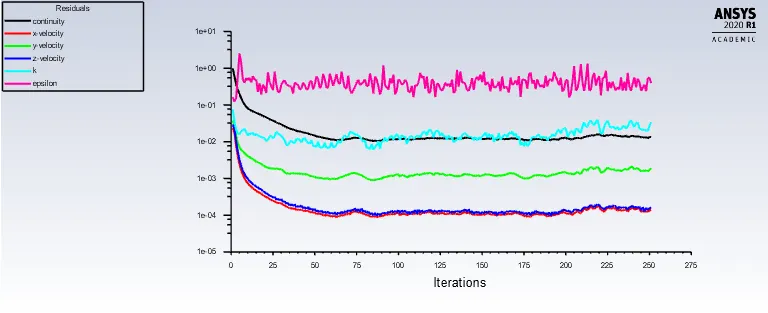
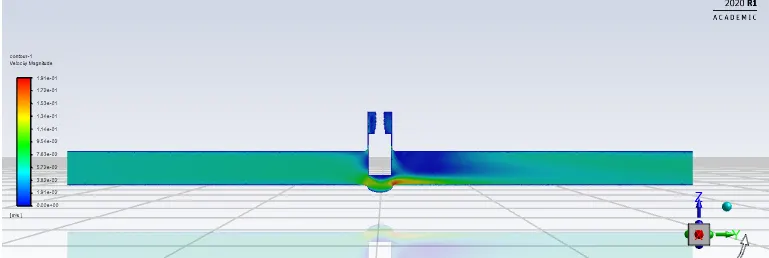
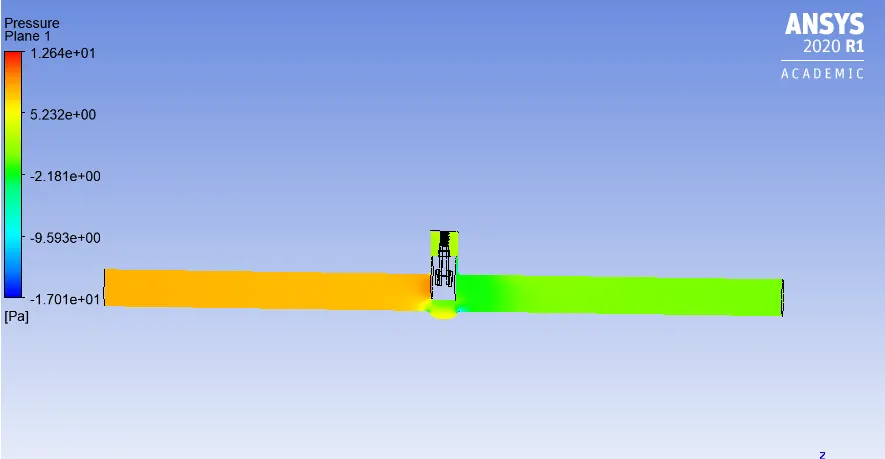
The results for the gate disc with 40mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
3. Velocity Contour
4. Pressure Contour
The results for the gate disc with 50mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
3. Velocity Contour
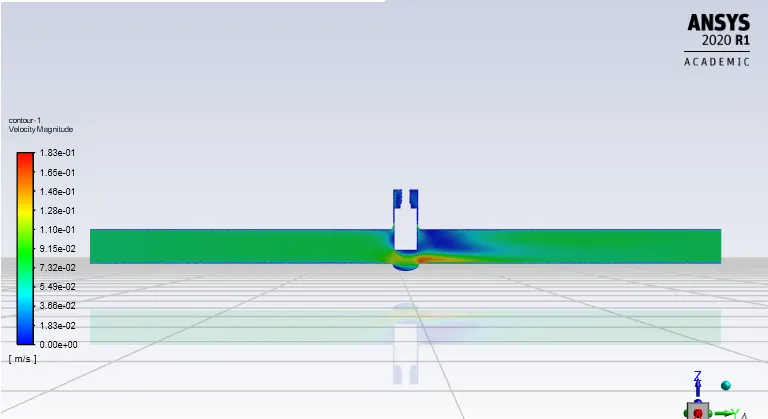
4. Pressure Contour
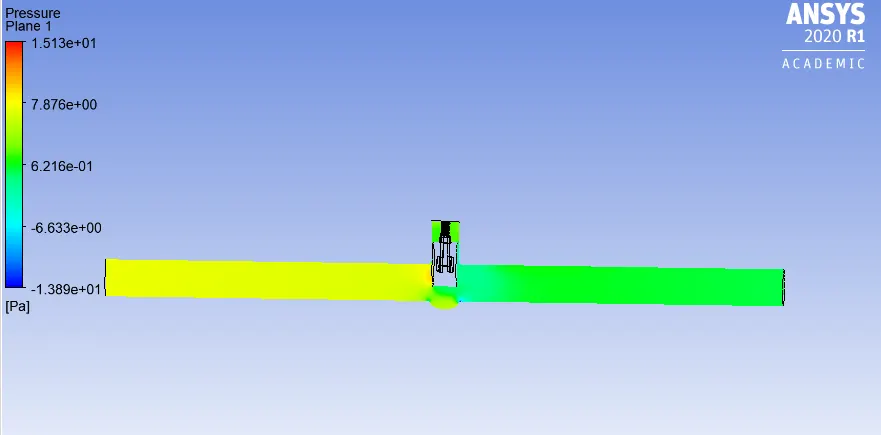
The results for the gate disc with 60mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
3. Velocity Contour
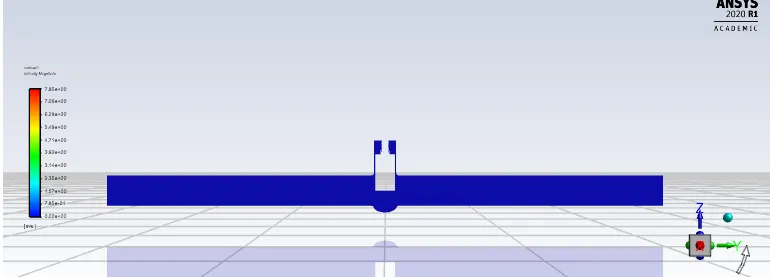
4. Pressure Contour
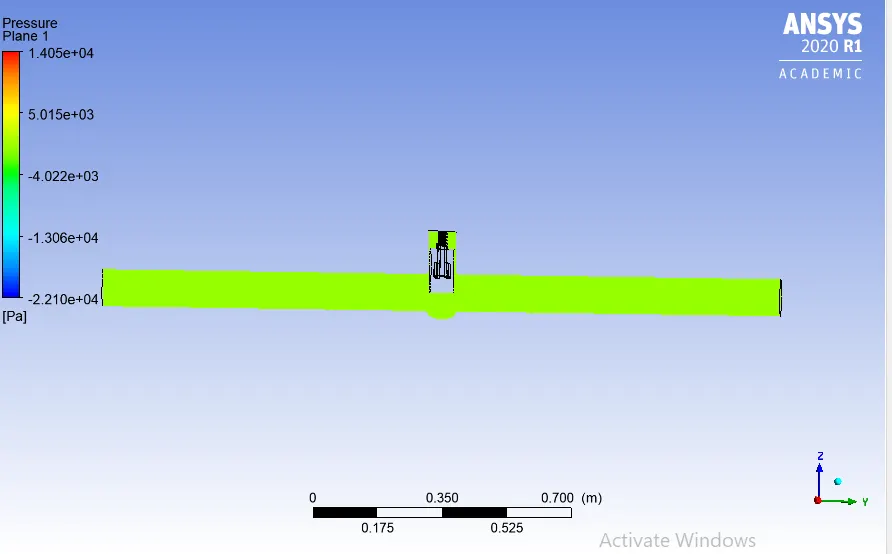
The results for the gate disc with 70mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
3. Velocity Contour
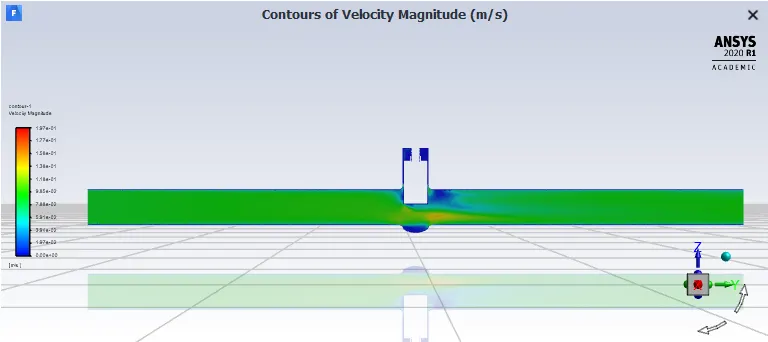
4. Pressure Contour
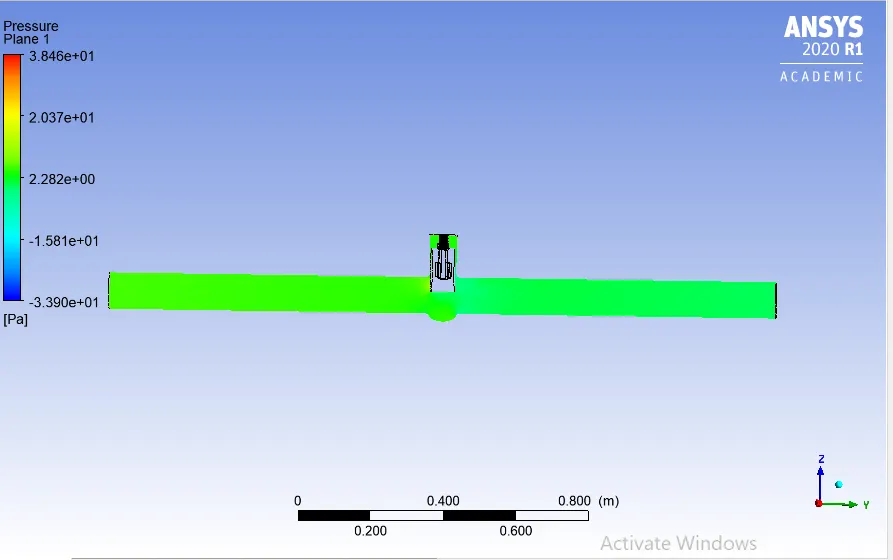
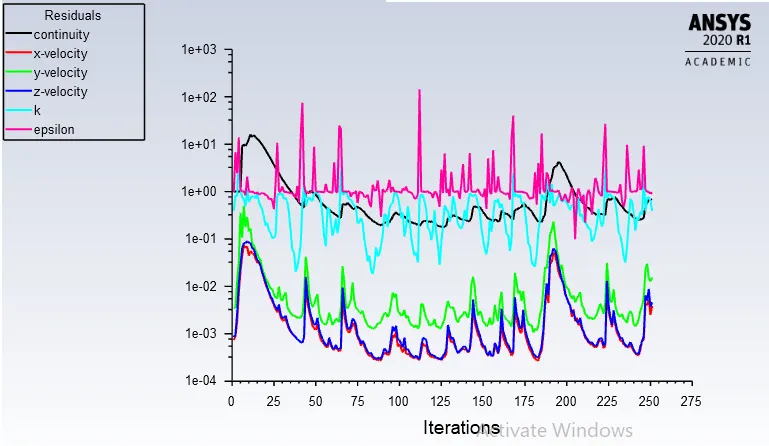
The results for the gate disc with 80mm lift can be seen below:
1. Residuals
2. Mass Flow rate at Outlet
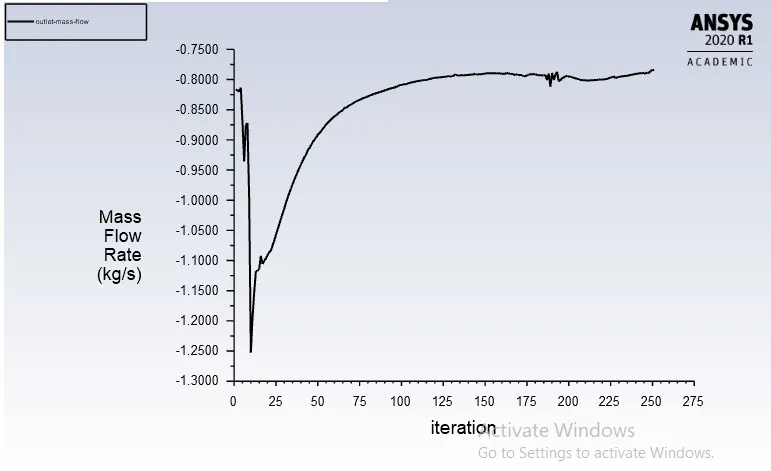
3. Velocity Contour
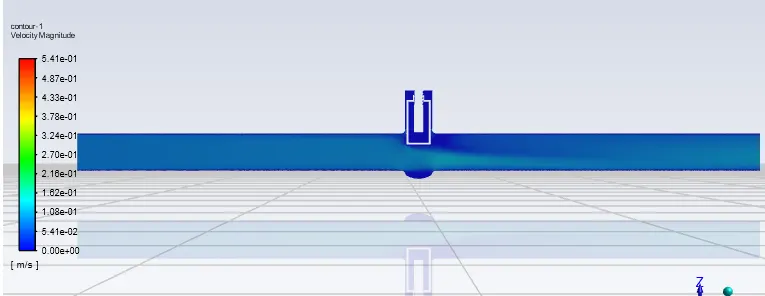
4. Pressure Contour
Flow Factor(Kv):
Flow factor is the flow coefficient in the metric units. It is basically defined as the flow rate in cubic meters per hour for water at the constantr temperature of 16 degree celcius with the pressure drop of 1bar across the valve.
The flow coefficient(Cv) of a device is a relative measure of its efficiency at allowing fluid flow. It describes the relationship between the pressure drop across an orifice valve or other assembly and the corresponding flow rate.
The flow coefficient can be defined as :
`k=Qsqrt(frac{Sunderset(g)()}{Delta P)`
where,
k= flow coefficient in Kv or Cv
Q= flow rate
Sg = specific gravity (1 for water)
ΔP= Total Pressure Drop
Simply Cv=Kv*1.156
The mass flow rate for design points can be seen below:
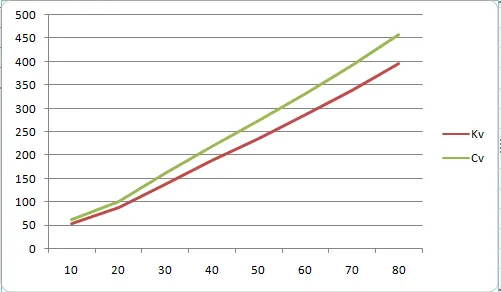
Here x axis represents the opening of the gate valve and the y axis represents the value of Kv and Cv.
Here it can be noticed that as the lift heifght increses the pressure drop also decreases and the flow coefficient also increases. Further high flow coefficient offers less frictionoll losses and the high pressure flow through the valve with very low pressure drop.
Conclusions:
- The low lift height refers to the higher pressure drop and thus low flow rate through the valve.
- The negative mass flow is due to the mass exiting the outlet.
- With the help of the parameters the solving time and effort can be reduced drastically.
- Flow factor and coefficient increses as the mass flow rate through the valve increases.