Week 9 - Attachment Feature Creation (Ribs & Screw Boss) - Challenge 1
Aim : To create the rib & screw bosses for the Drill Handle considering the design rules
- To create the tooling axis for the given Class-A Surface meeting the requirements of the draft angle and at the end perform the Draft analysis on the final model.
Design Methodology:
The input of the product designer is in the form of the Class A Surface. The job of the product designer is to create the B and C surfaces and then creating the ribs and screw bosses on the solid body by keeping all the aspects for the mold.
Creation of Tooling Axis:
The tooling axis is the direction of drawing a sheet metal where the finished component is easily ejected on a particular direction and axis. In Molding, machine arrangement is given to open the mould along a direction which is known as Tooling Direction. In other words. The mould is built from two separate halves (Core and Cavity) and tooling direction basically defines the direction of mould pulls apart.
In the given model we are using the Normal To Surface method.
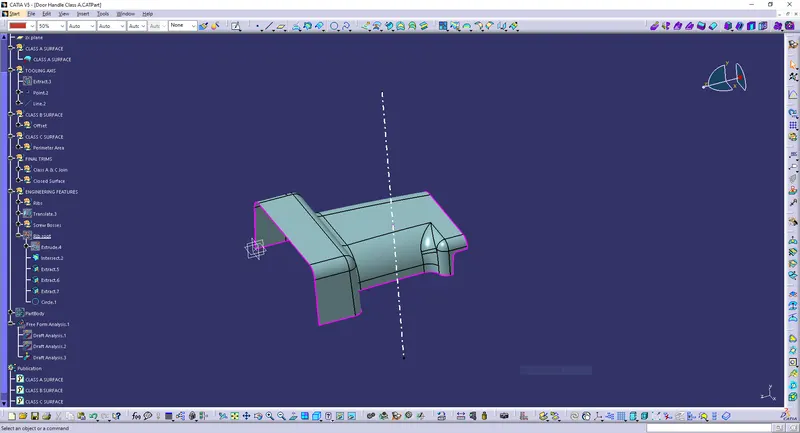
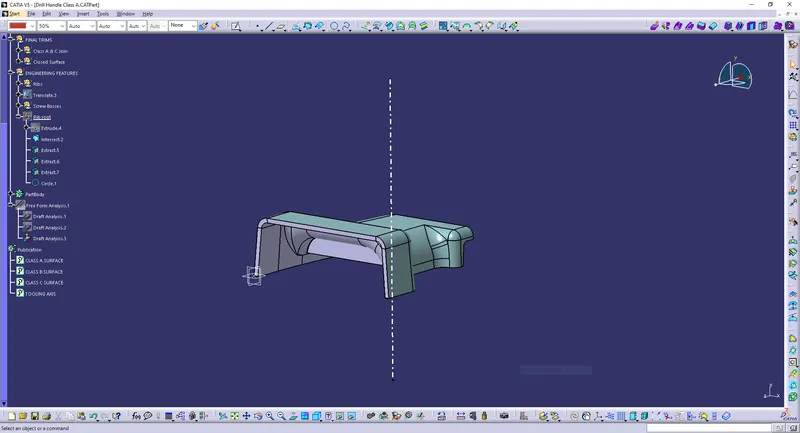
For creation of tooling axis, a point is inserted on one of the surface of class A through which tooling axis is drawn.
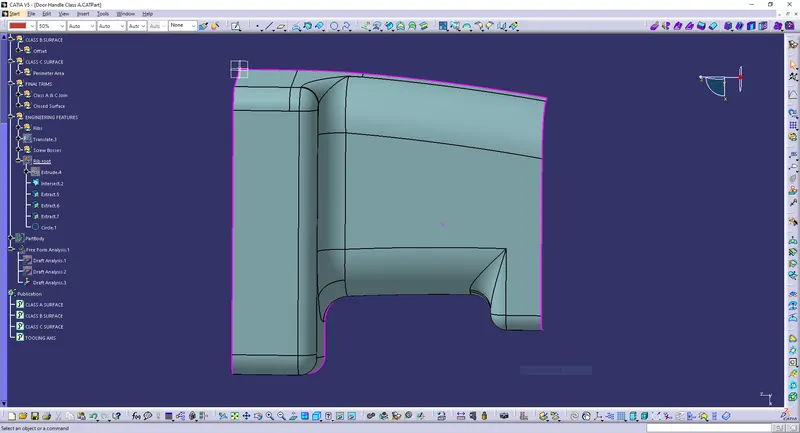
Class A surface with point on the surface:
Class A surface with Tooling Axis:
Material Selection
The material can be used for manufacturing Drill Handle is Acrylonitrile Butadiene Styrene (ABS). Because of its some features such as:
- The styrene provides the copolymer with a shiny, tough exterior.
- Provides quality surfaces and good resistance to chemical agents.
- A wide variety of adjustments can be made to enhance impact resistance, durability and heat resistance.
Also the Polyoxymethylene material can be used to manufacture the Door trim. It has the features called: high rigidity, yield strength and high stability in cold temperatures. Highly chemical- and fuel-resistant. Also POM is used to fabricate interior and exterior trims.
For manufacturing Door Trim component the injection molding method can be adopted. It would be the right manufacturing method. Because it is a right way to create the exact moulding for the required product. This is a common method is used to produce a high volume of plastic parts of automobiles. Products can also be made with increased flexibility to suit the needs of designers or engineers.
Class A,B & C Surface
Class A Surface:
It is the outermost aesthetic surface which is visible to customers (the outermost visible surface of a product).
Here, class A surface is given:
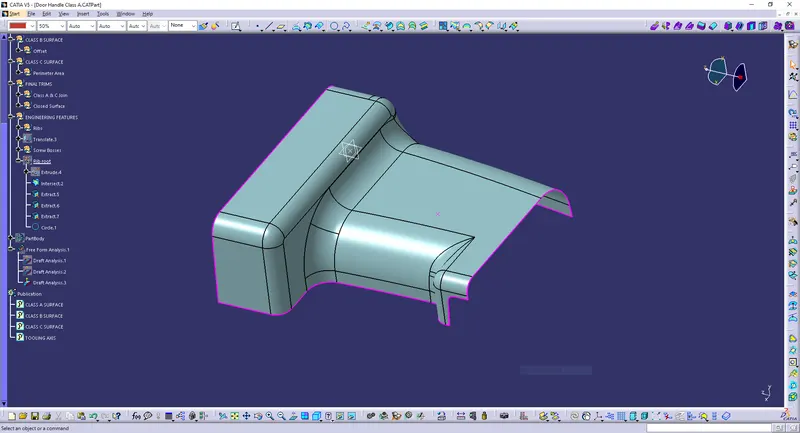
The class A surface is joined inorder to make it a single part and then checked the boundary to confirm that it is closed.
Class B Surface:
It is the offset of the class A surface at a particular distance. The offset distance depends on the thickness between Class A and Class B surface.
Here, the thickness given = 2.5mm.
Procedures to build class B surface:
- Offsetted the joined surfaces from class A to 2.5mm inorder to create class B surface.
- Extrapolated the offseted surfaces inorder to make sure all the surfaces are in contact.
- Trimmed the offsets to get an output same as class A surface
- Fillets are given to the required edges based on the thickness and curvature of the class A fillets.
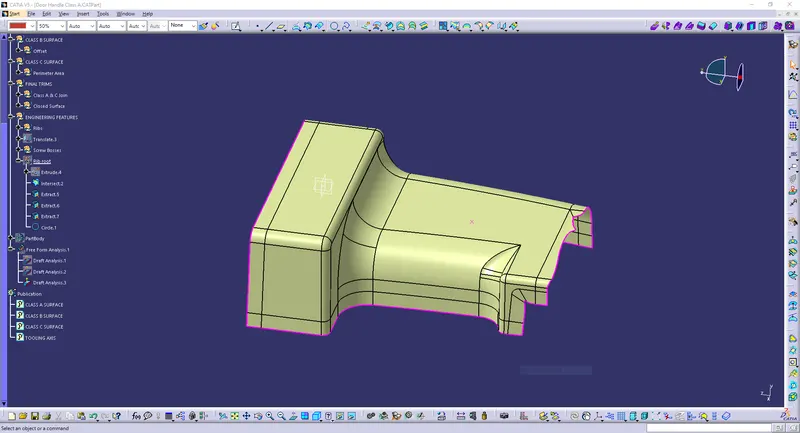
Class C Surface:
This surface connects the Class A and Class B surfaces. (Surface in between Class A & B surfaces)
Procedure to build Class C surface:
- Boundary of class A surface is extracted and then smoothcurved the boundaries if its required
- Also here Multi-Section Surface command is used to create the Class C Surface
- Both the sweep surface and multi-section surface are joined together to form as a single one.
- Then that boundary is swept perpendicular to the Class A Surface until it gets coincided with the offseted class B surface.
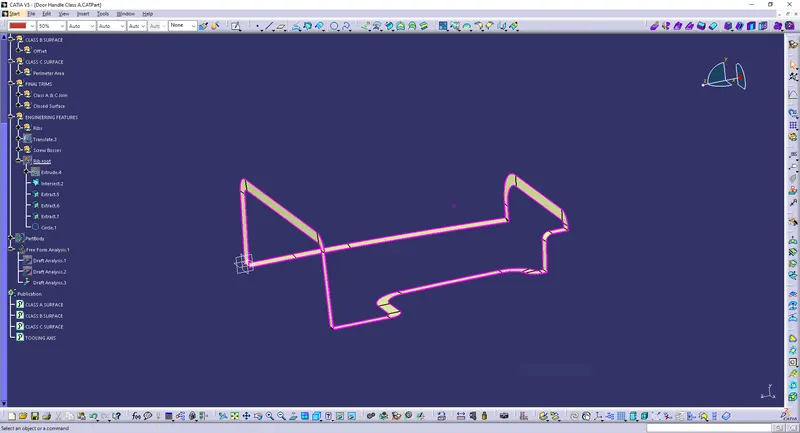
Joined and Closed Class A,B & C surface:
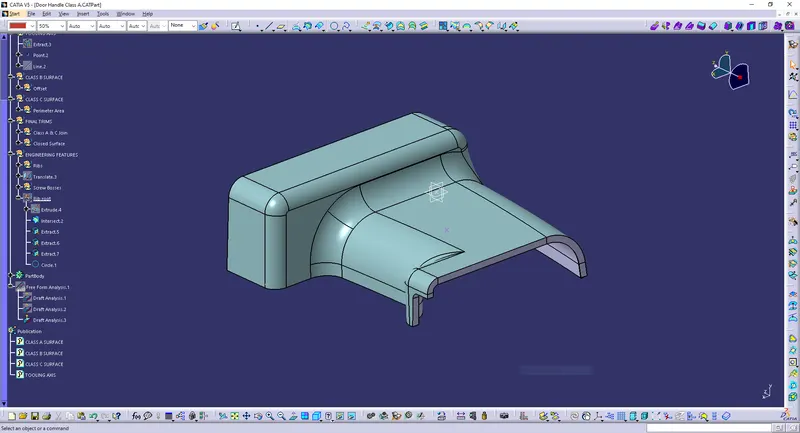
After creating class B & C surfaces, joining operation is done between class A and class C surfaces. Then, Class B surface is trimmed with joined Class A & C surfaces to get a whole closed single surface. Then in the part workbench using closed body command, a solid body is generated.
Closed surface:
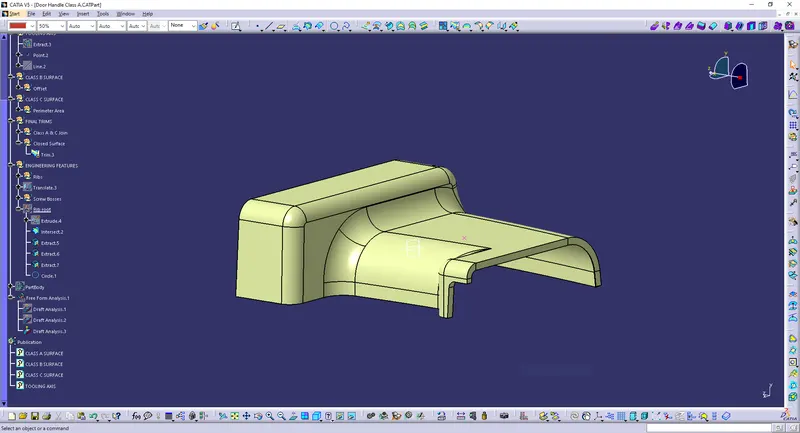
Solid Body:
Attachment of Engineering Features:
RIBS:
Ribs are usually designed to Improve Strength of Plastic Part without increasing the thickness of the component.
Design Principle for Rib Creation
-
Ribs are thin wall protrusions that extend perpendicularly from a wall or plane. They are usually found in clusters offering support to a plane that would have otherwise been too thick, but can also be stand-alone support for a single wall. They are commonly used to provide additional support and strength to a part. Thickness and location are essential to rib design.
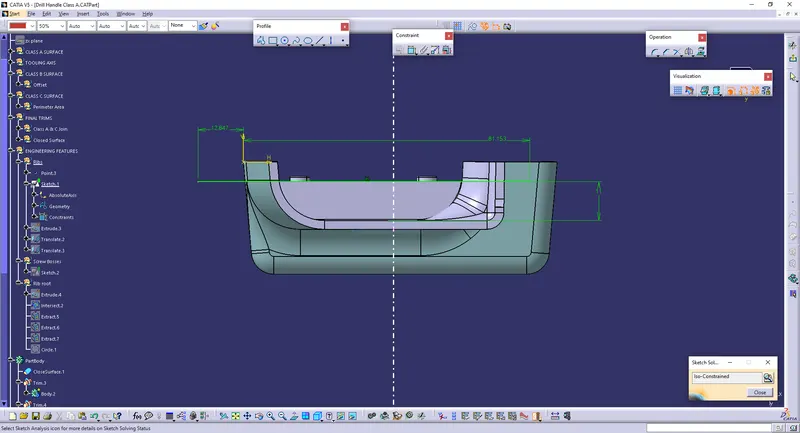
First, the base surface where the rib has to be created is extracted using the Extract command. A positioned sketch is created and the profile for the rib is drawn.
-
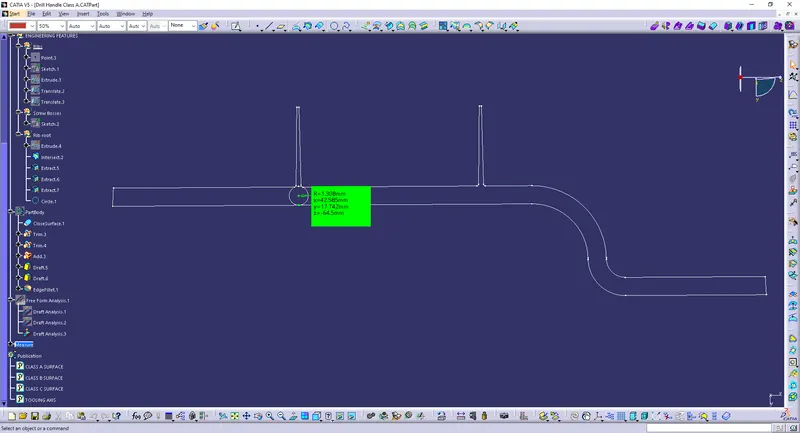
Next, the profile is extruded, to find the height,h=Wall thickness * 4.4
=2.5*4.4
= 11mm
Therefore, the height is 11mm
-
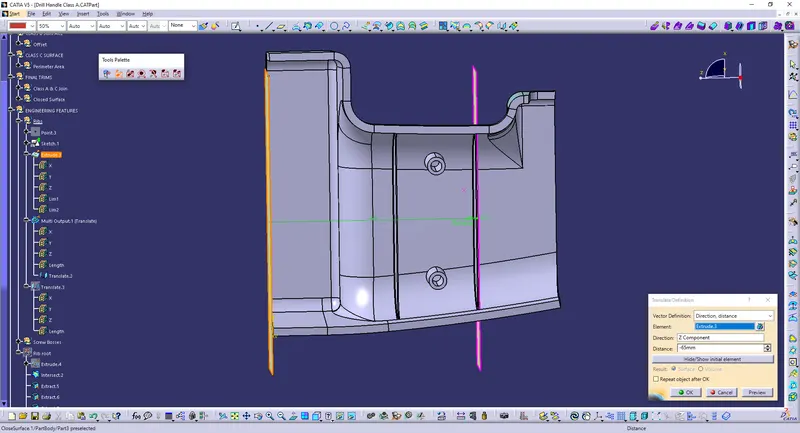
The extruded surface is thickened,
Thickness,w=0.4*t
=0.4*2.5
=1mm
Therefore, the thickness of the rib is 1 mm.
Rib Root Thickness:
Screw Boss:
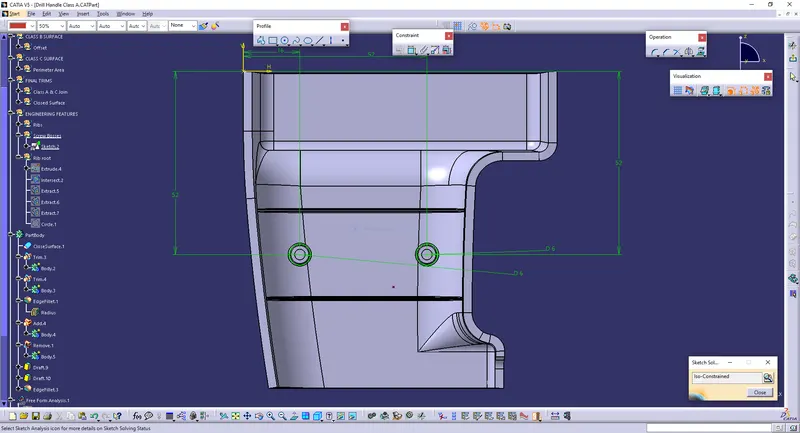
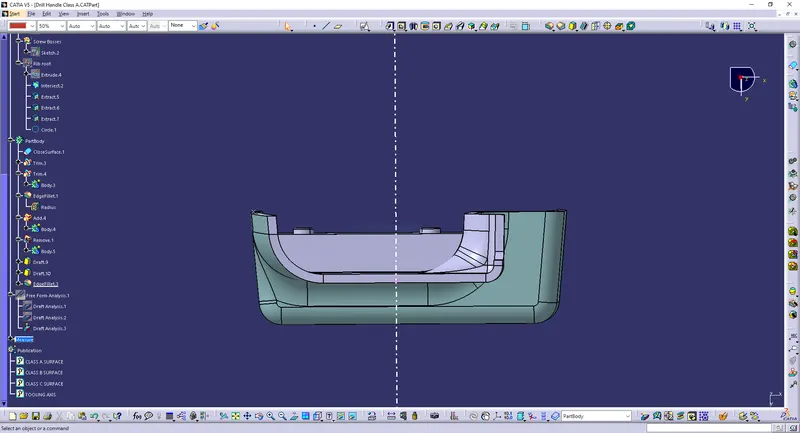
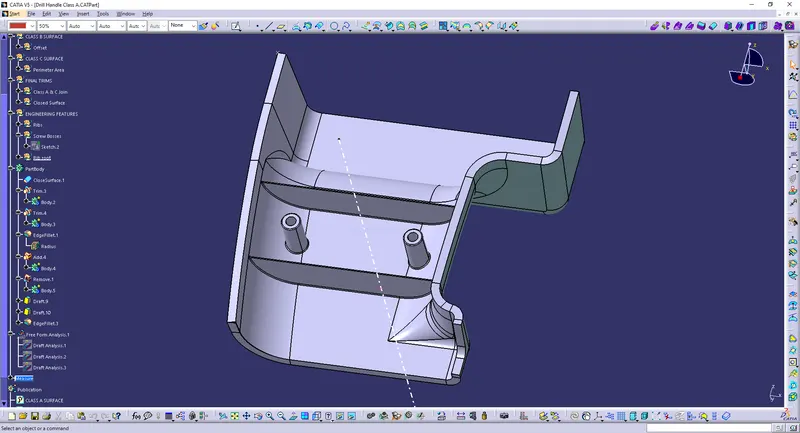
It helps to screw component together. Screws are secondary features which is on B surface. Bosses are used to attached & assembly features of many components.
Draft Analysis:
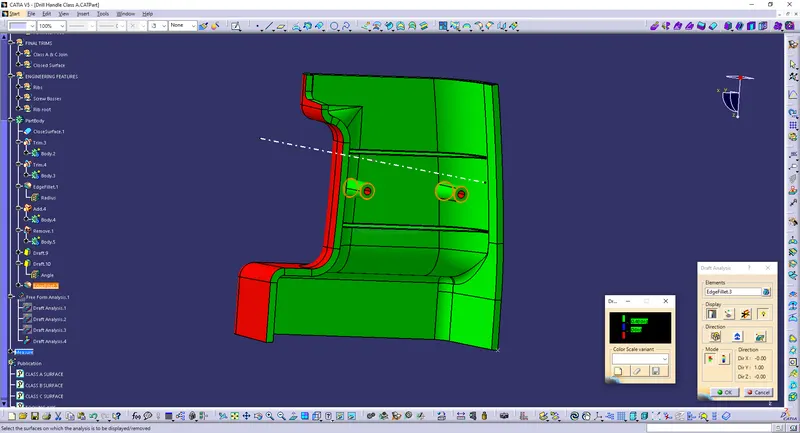
In the criteria of making a plastic material, the mold should release the material when finished. if the mold surfaces are 90 degrees the material won't release from the mold because of friction due to contraction of material when cooled.The ejection of the part from mold depends on the draft. A zero draft can result in difficult or no ejection. It is recommended to add a draft of 3 degree or above inorder to remove it from the mold without any damage.
Procedure:
- Change the view mode to customize view parameters and give material as view mode.
- In the draft analysis toolbar, set the draft values and color (3 degree and above - green, 0 to 3 degree - blue, less than 0 - red).
- Drag and drop the axis system on the tooling axis and lock it.
- Perform draft analysis.
Draft analysis of Class A surface:
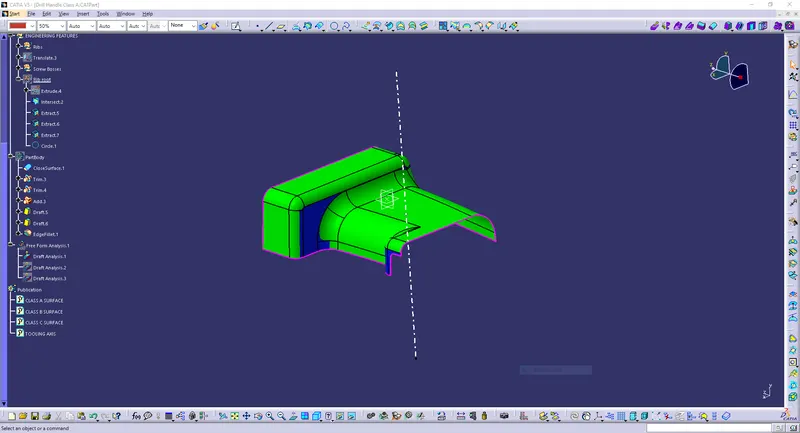
It is clearly shows that the above figure with is having blue colour in some of its area. Thus the blue coloured area is with draft angle less than 3 degree. Hence to eliminate this the Class A Surface is to be modified.
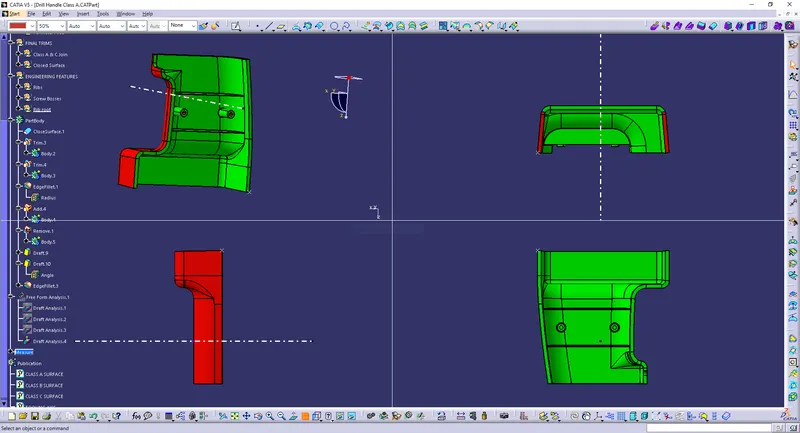
Draft analysis of final component:
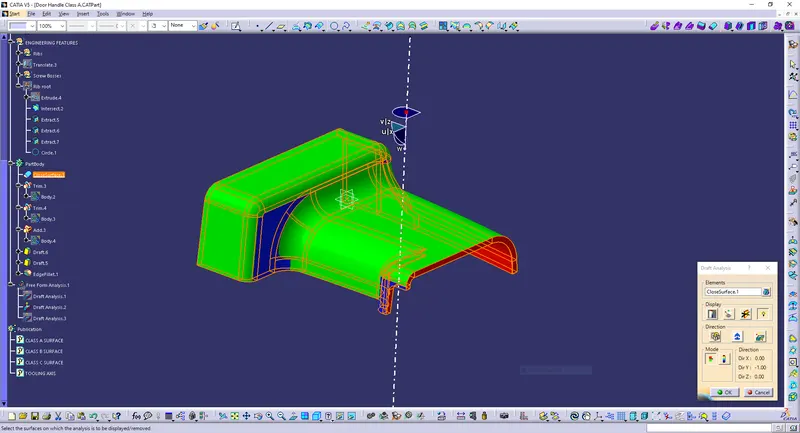
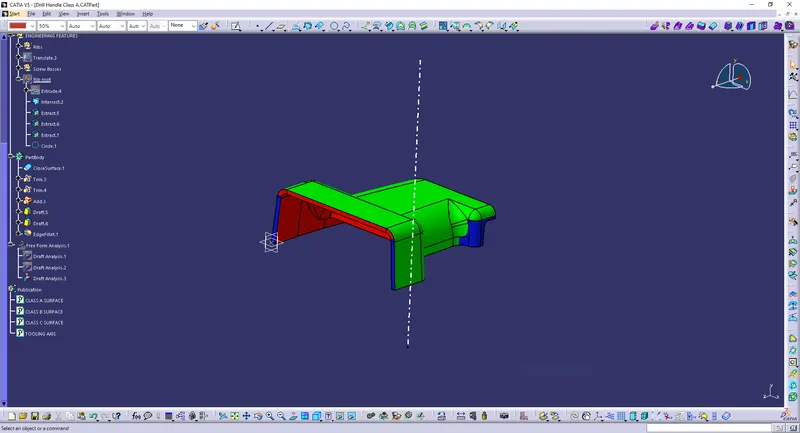
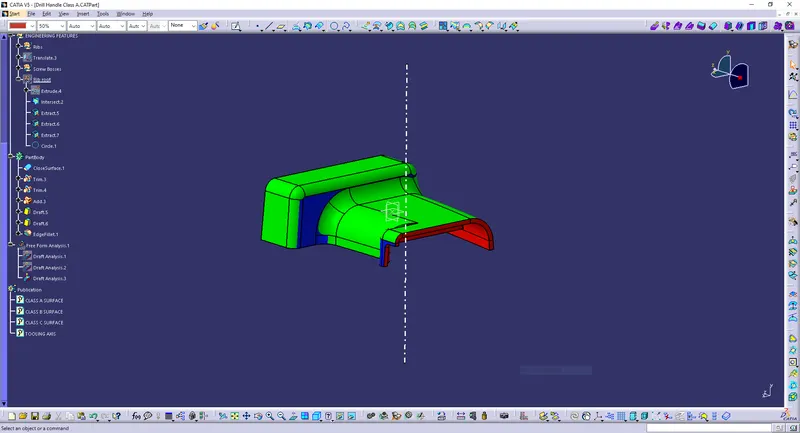
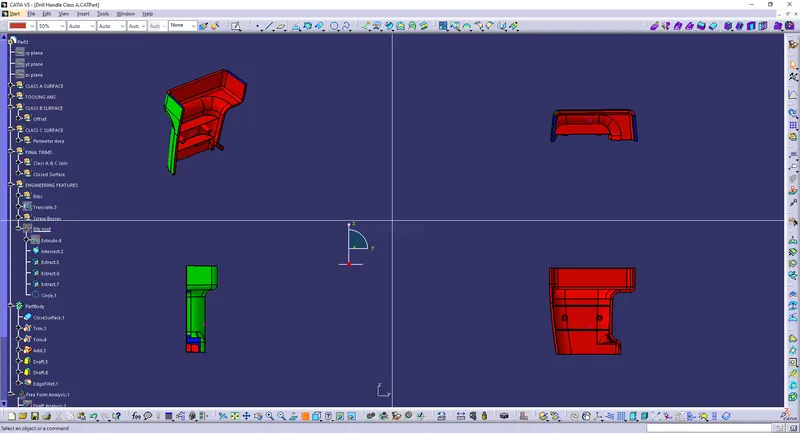
After changing the draft angle to 0.48 degree on draft analysis. Hence it will clear on the draft analysis and can be manufactured.