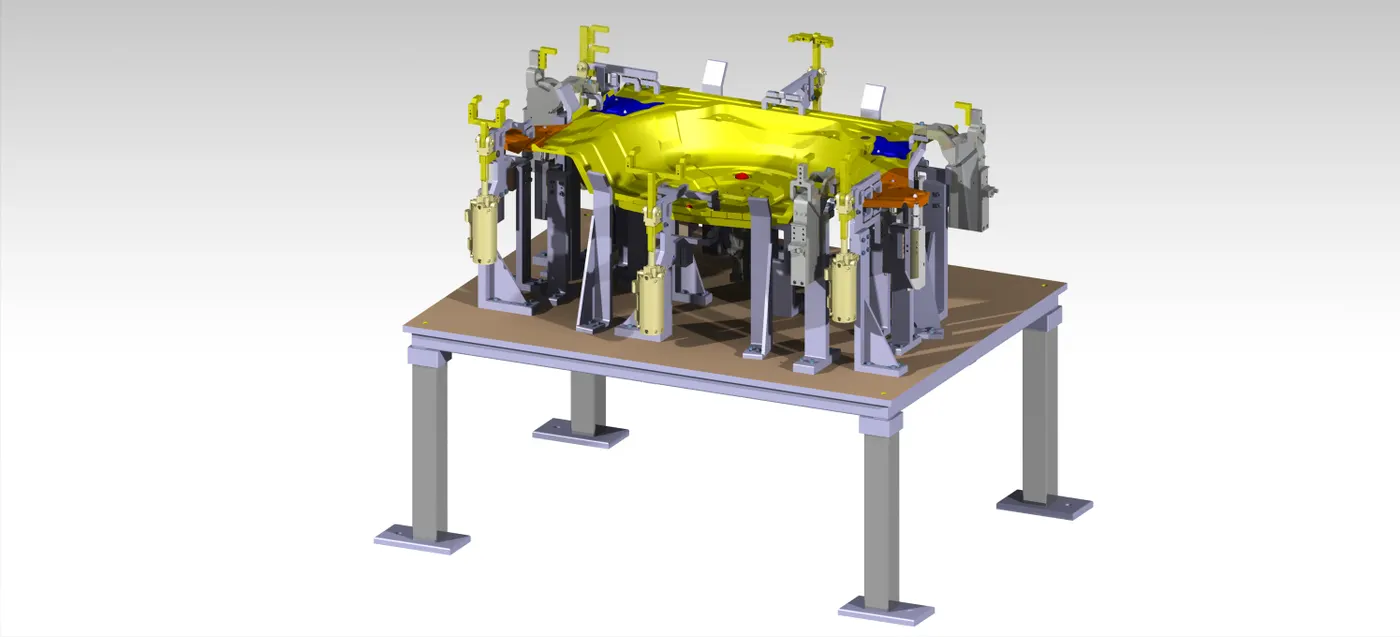
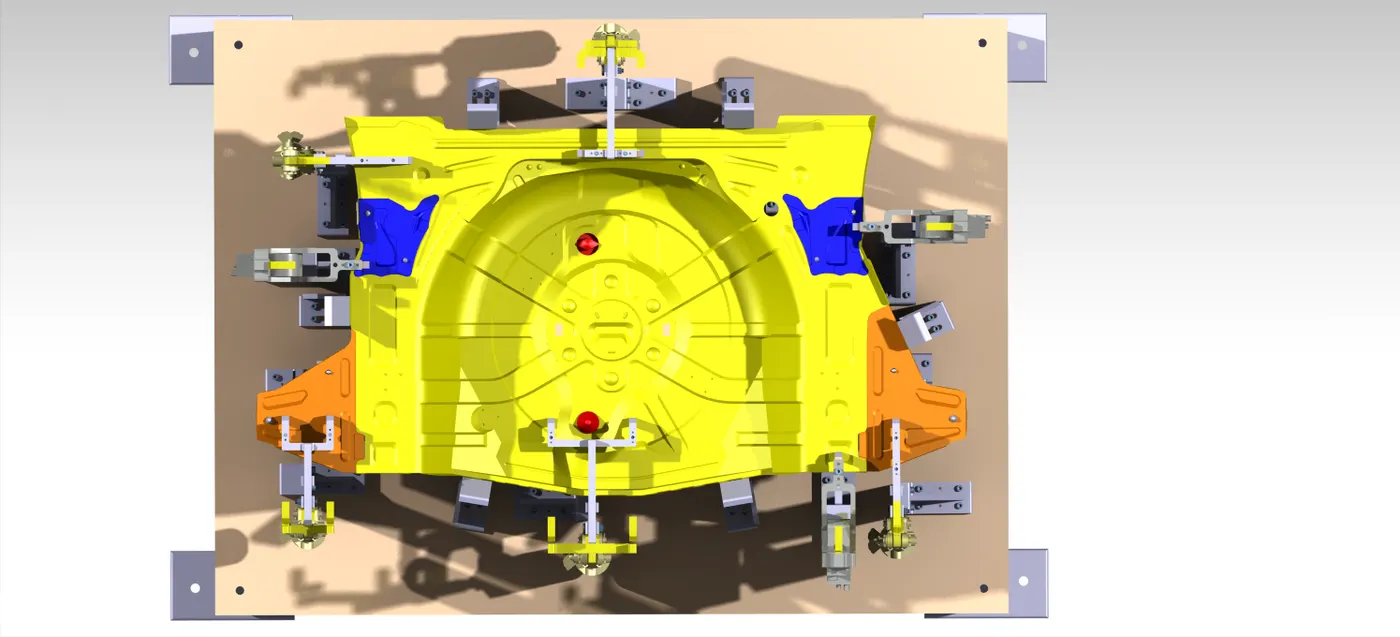
Week 8:- 3D Finishing Challenge 2
AIM:
- Perform 3D finish for all units of Assembly design.
- Create Rough locators for Assembly.
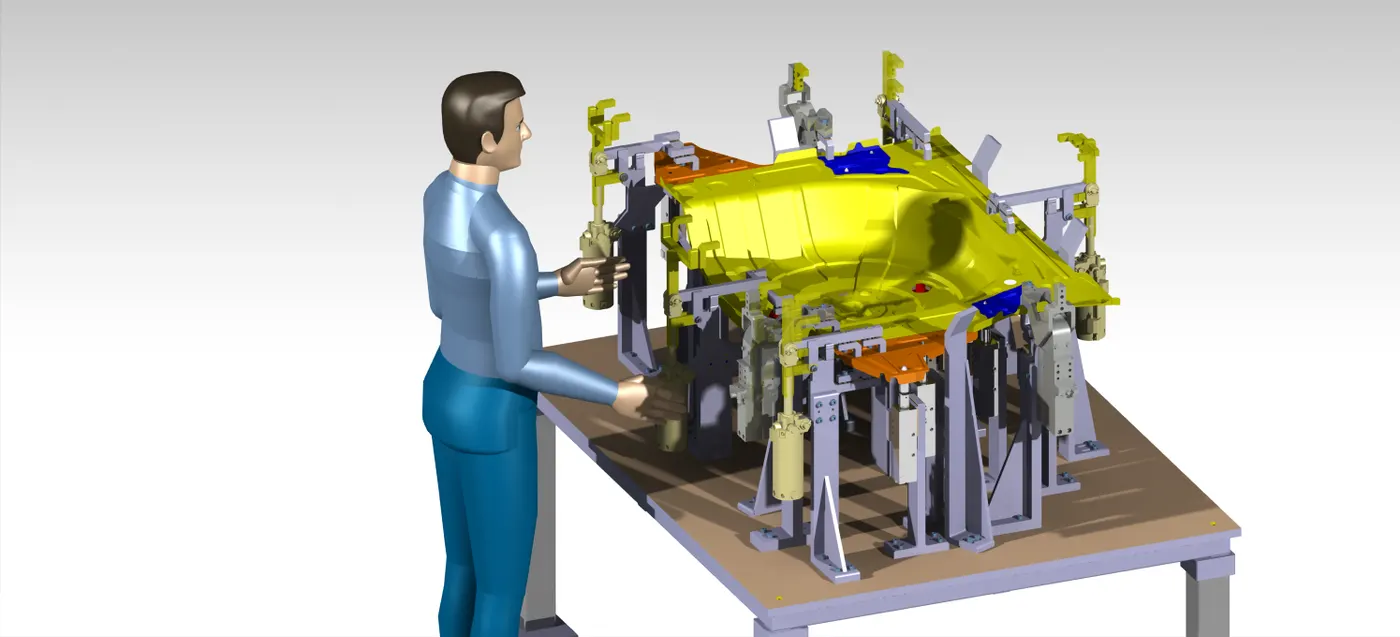
3D FINISH:
The 3D finish is the process where design is completely finishing & to be ready for final simulation & 2D detailing
- In 3D finishing we perform and ensure the following points:
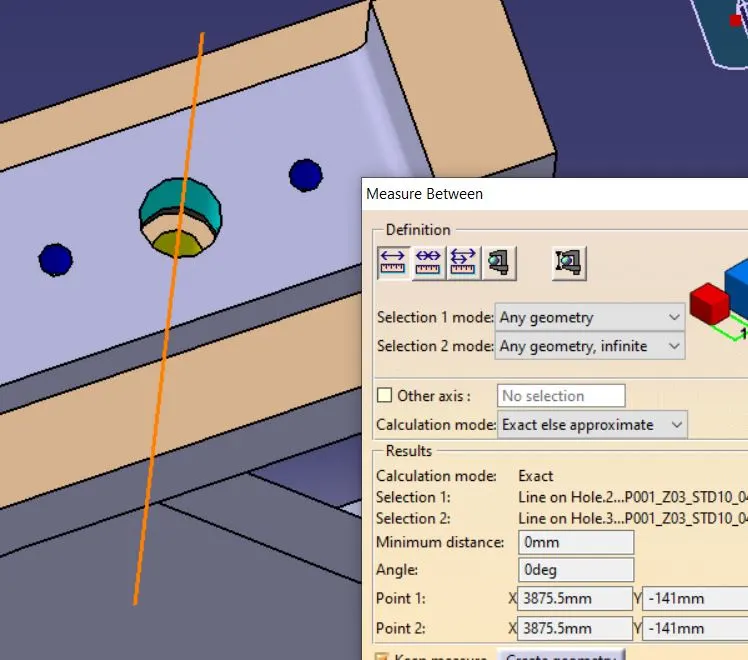
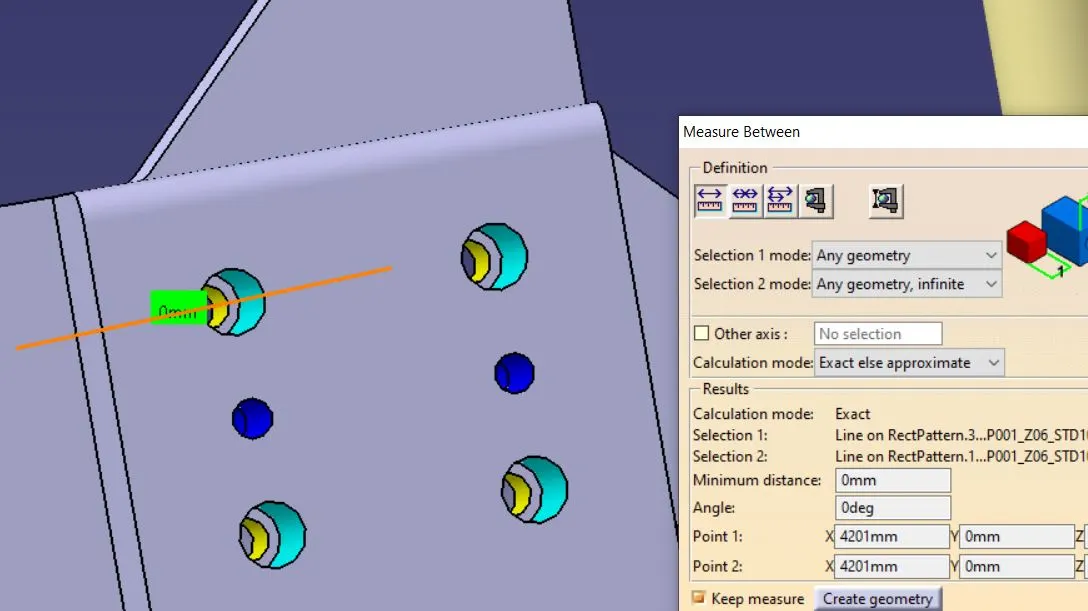
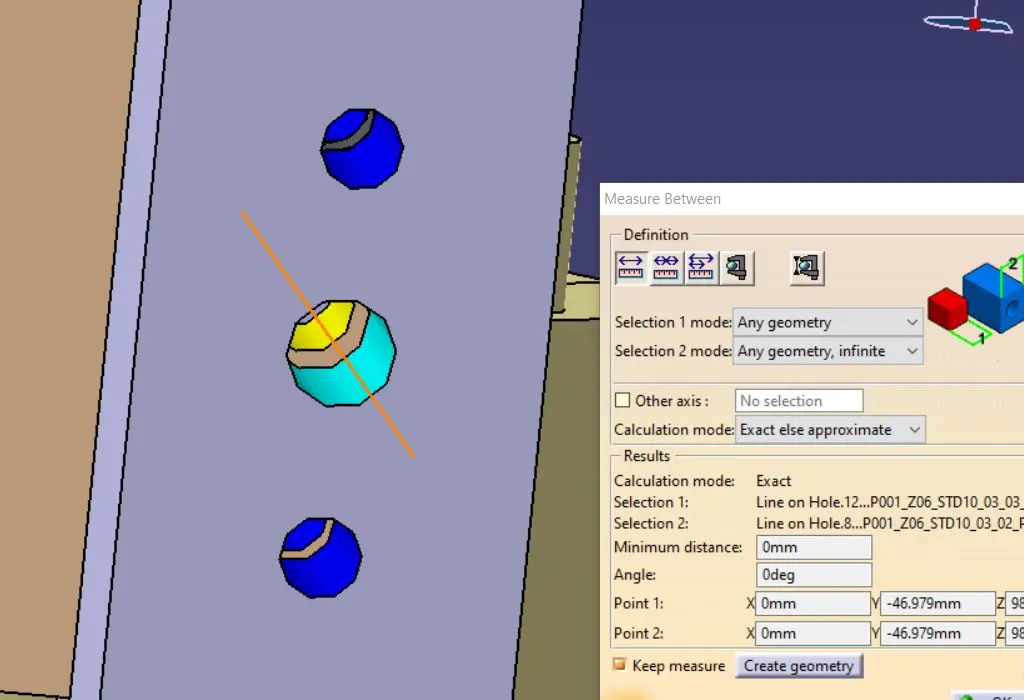
- Hole concentricity & hole sizes- All parts Hole concentricity is checked & confirmed while finishing the parts.
- Machining Area- The machining area in every part is defined & the machining area is highlighted by using orange colour.
- Nominality- All units dimensions are maintained nominal to facilitate easy assembly of the unit.
- Holes colouring standard- Color Code standard used in the 3D finishing
- Cyan - Simple Hole
- Yellow - Threaded Hole
- Orange - Machined area
- Blue - Dowel pin Hole
- Fasteners implementation- Fasteners are implemented in all unit as per the requirement & load on the part.
- Avoiding clash between different part- Proper gap is maintained between parts to avoid the clash.
- Mylar splitting as per panel profile- Mylar splitting are confirmed while finishing the design.
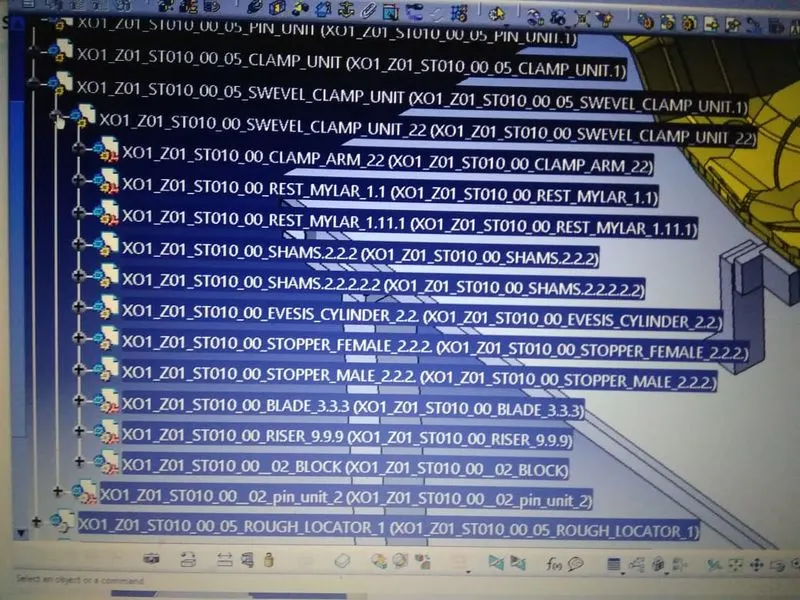
- Proper renaming of parts/assemblies as per standard-proper renaming of parts & assemblies are done while finishing the design hence we can identify each & every part easily with a unique identification.
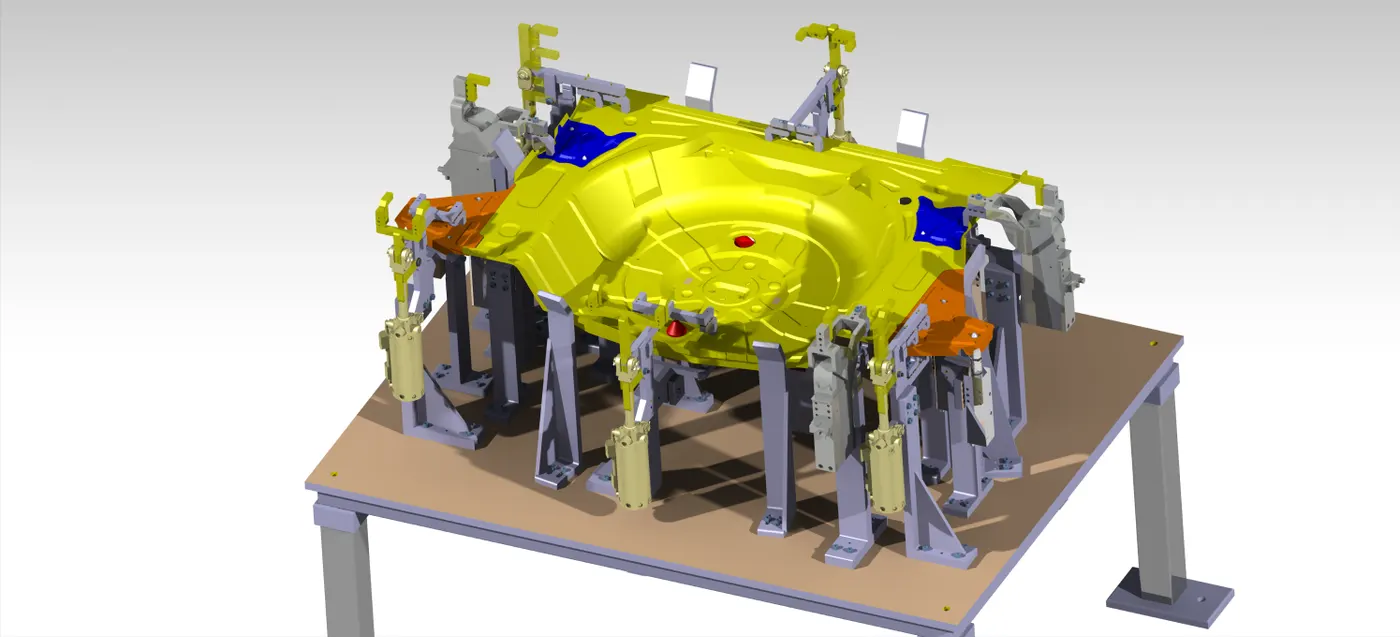
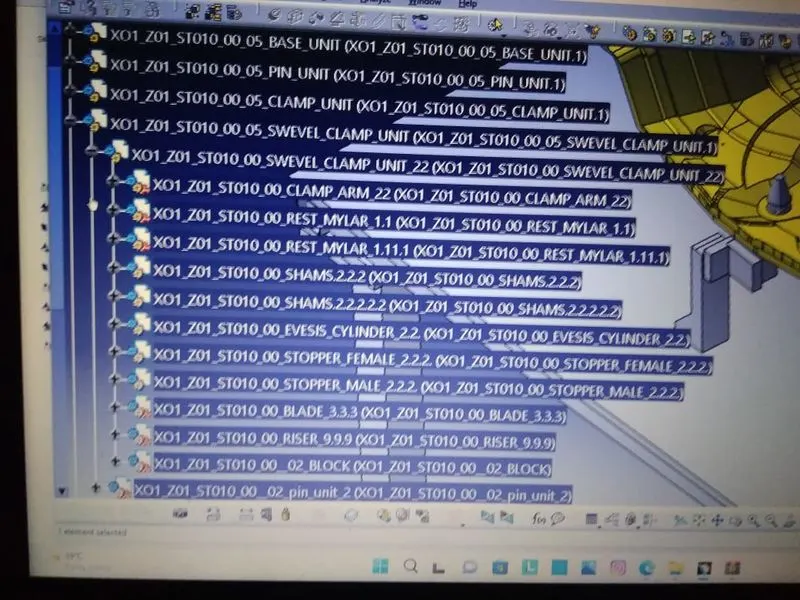
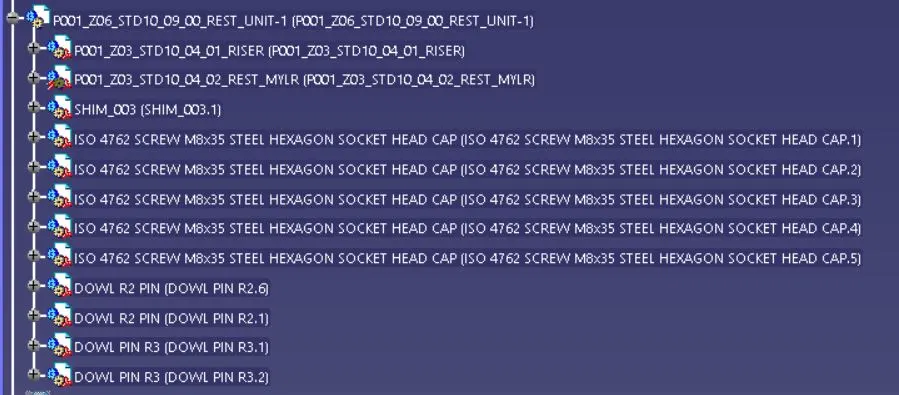
1 Renaming and Structuring of the design tree:
- Renaming of the design tree is done. and structuring design tree in way that its simple to identify the units. some units use multiple time those are easy to identify by its name.
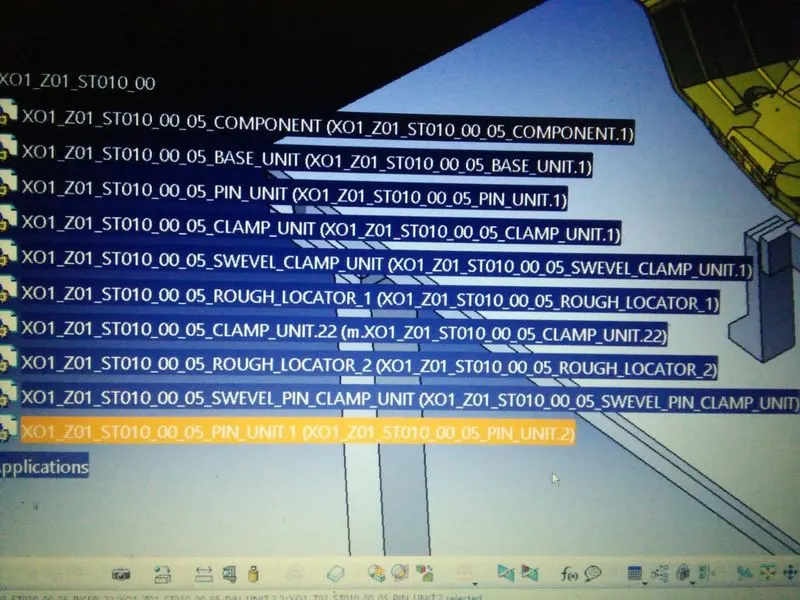
fig- Renaming of all parts.
2 Base Unit:
- Renaming of parts and structuring design tree
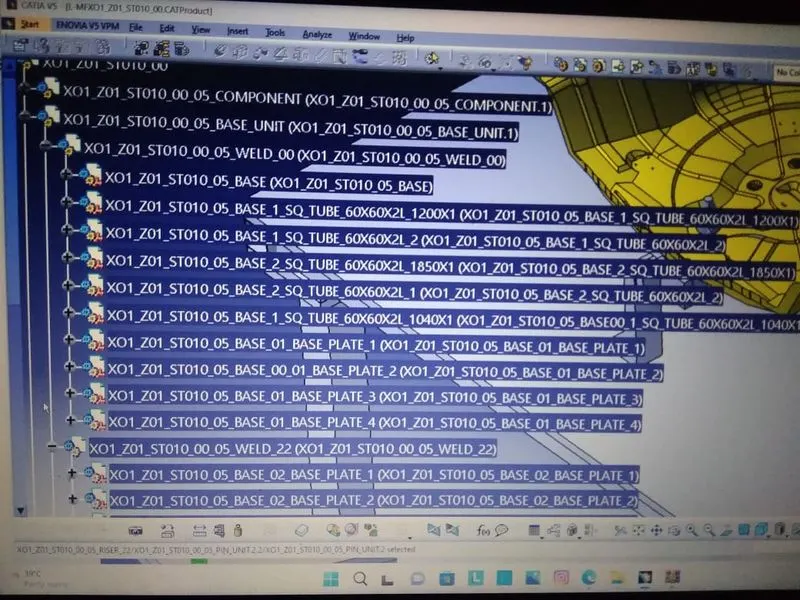
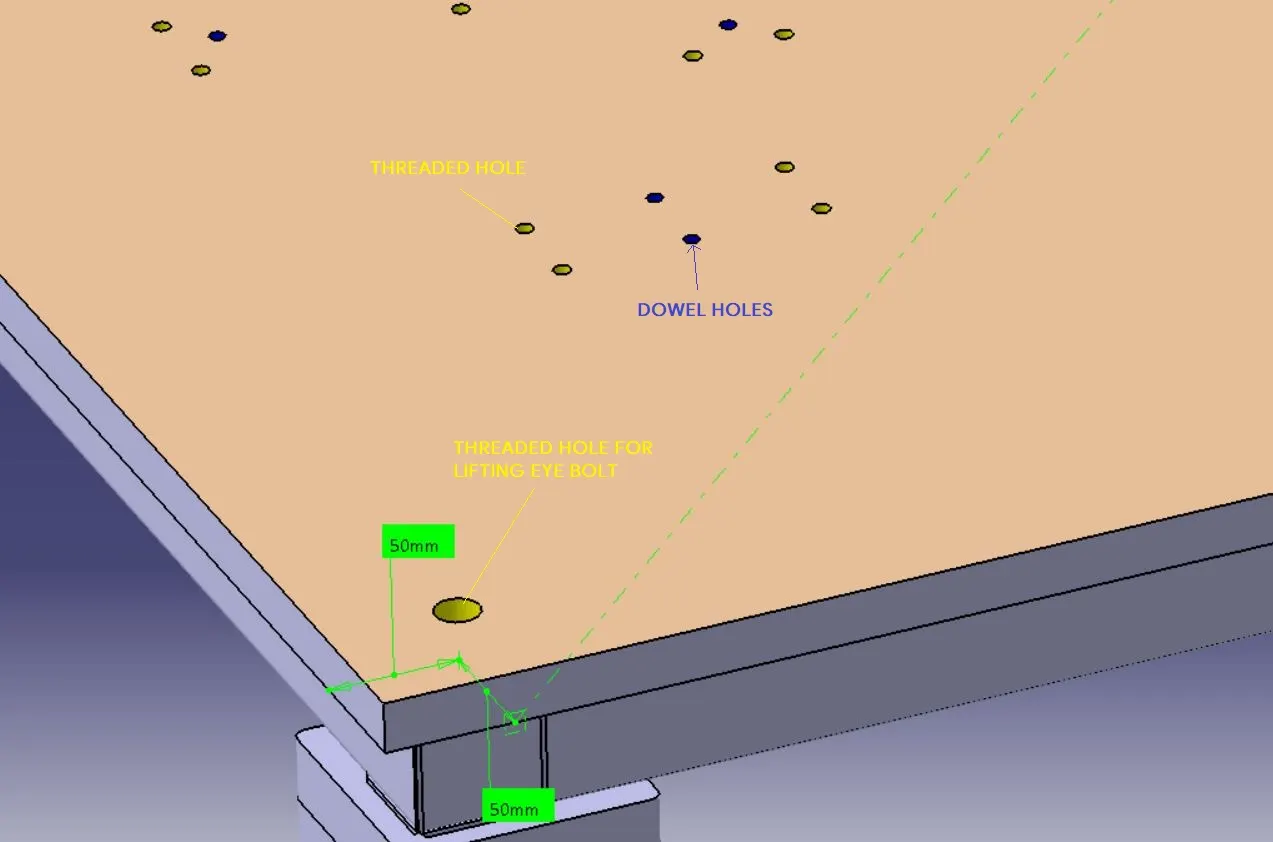
- Threaded hole and dowel holes making nominal and colour-coding are done so easy to distinguish holes.
- Threaded hole (Yellow), clearance hole (Sky blue), Dowel Hole(Blue), Machining surface(orange
| Checking Parameter | Action |
| Rename of the design tree | Done |
| Mark Machining Area | Done |
| Nominality | Done |
| Holes colouring standard | Done |
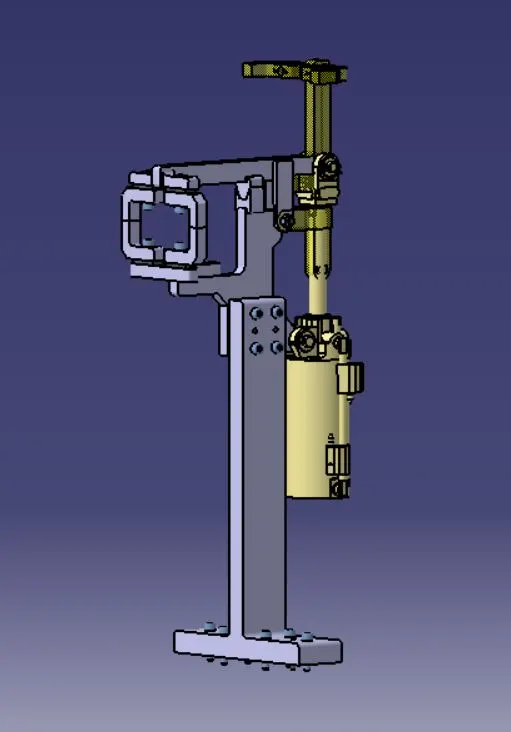
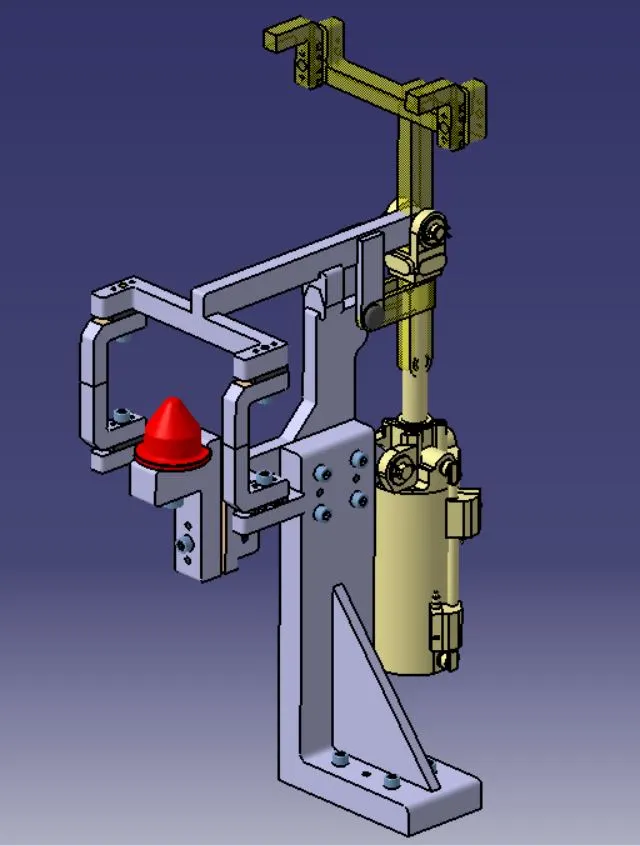
4 Swivel Clamp Unit
- Holes are make to the nominal and Concentric to each other.
- The proper butting of the two parts is done.
- fasteners are implemented.
- colour coding is done as per the standards.
- structuring design tree renaming of parts is done.
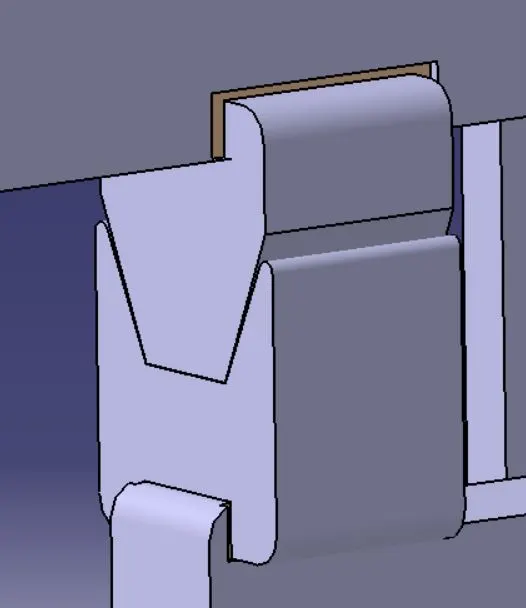
- mylar splitting is done.
- the open position is shown in yellow colour.
- below are some images after 3d finishing done on swivel Clamp unit.
XO1_Z01_ST010_00_05_CLAMP_UNIT.22
| Checking Parameter | Action |
| Rename of the design tree | Done |
| Mark Machining Area | Done |
| Nominality and Concentricity | Done |
| Holes colouring standard | Done |
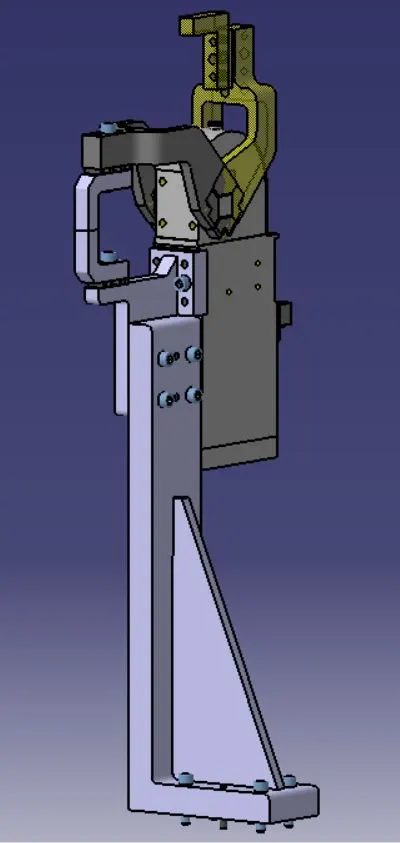
5 Power Clamp Unit
- Holes are make to the nominal and Concentric to each other.
- The proper butting of the two parts is done.
- fasteners are implemented.
- colour coding is done as per the standards.
- structuring design tree renaming of parts is done.
- mylar splitting is done.
- the open position is shown in yellow colour.
- below are some images after 3d finishing done on swivel Clamp unit.
XO1_Z01_ST010_00_05_SWEVEL_CLAMP_UNIT.1
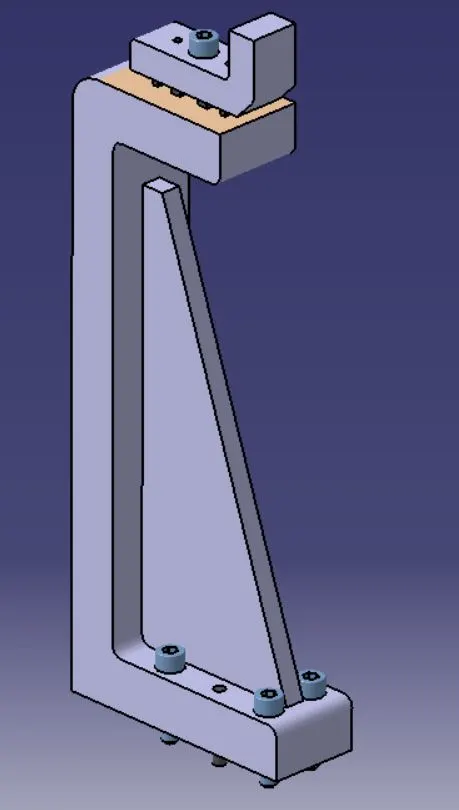
6 Rest Unit
- Holes are make to the nominal and Concentric to each other.
- The proper butting of the two parts is done.
- colour coding is done as per the standards.
- structuring design tree renaming of parts is done.
- mylar splitting is done.
- below are some images after 3d finishing done on swivel Clamp unit.
P001_Z06_STD10_09_00_REST_UNIT-1
| Checking Parameter | Action |
| Rename of the design tree | Done |
| Mark Machining Area | Done |
| Nominality and Concentricity | Done |
| Holes colouring standard | Done |
7 PIN CLAMP UNIT
- Holes are make to the nominal and Concentric to each other.
- The proper butting of the two parts is done.
- colour coding is done as per the standards.
- structuring design tree renaming of parts is done.
- mylar splitting is done.
- below are some images after 3d finishing done on swivel Clamp unit.
 v
| Checking Parameter | Action |
| Rename of the design tree | Done |
| Mark Machining Area | Done |
| Nominality and Concentricity | Done |
| Holes colouring standard | Done |
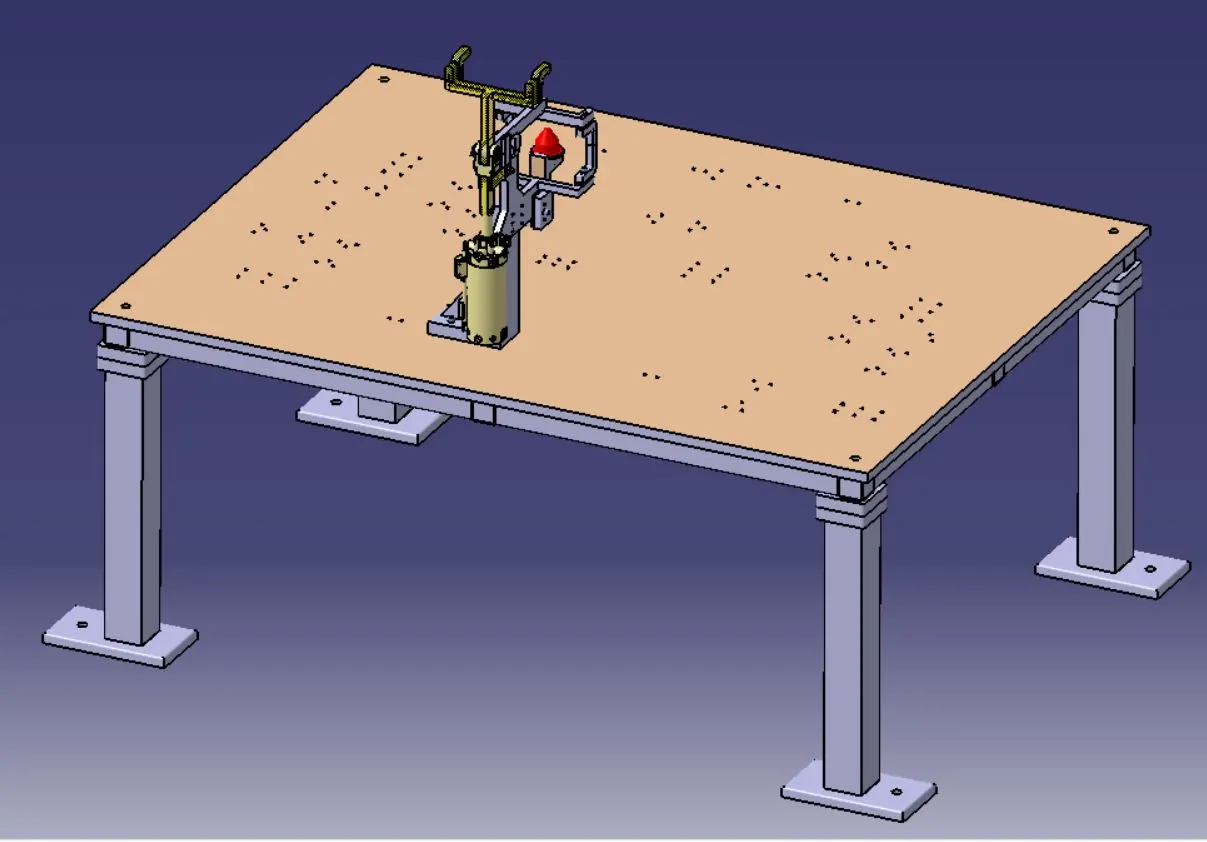
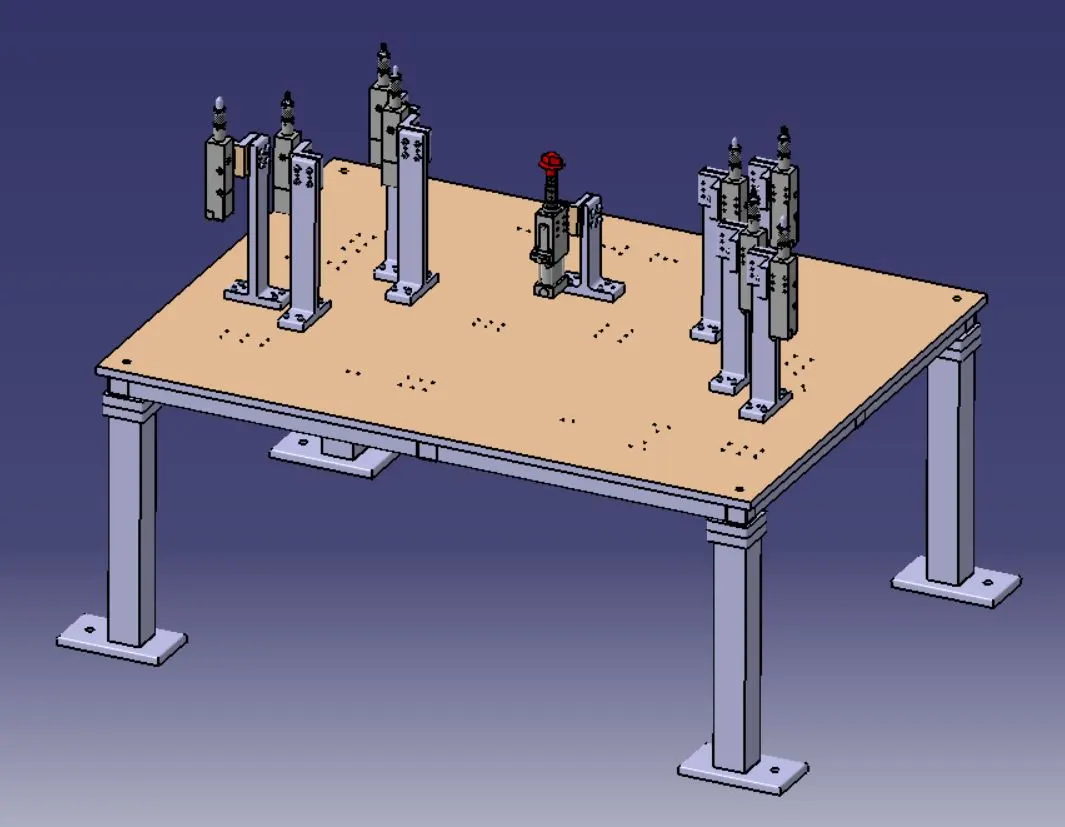
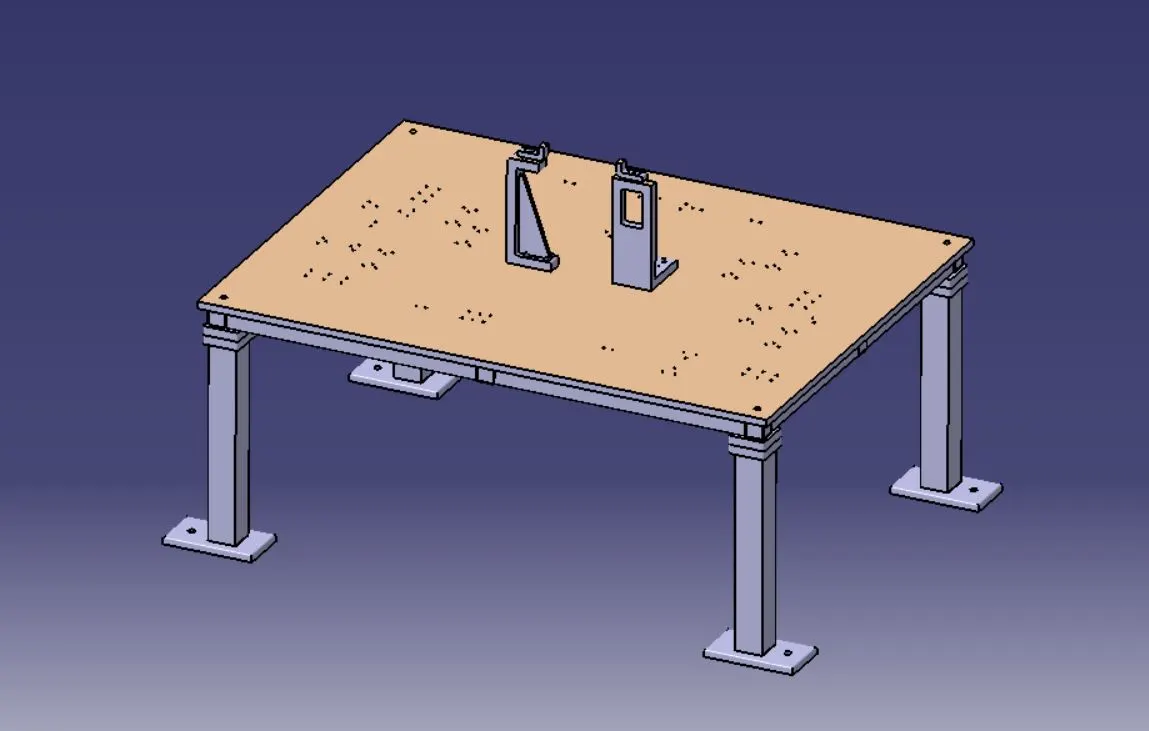
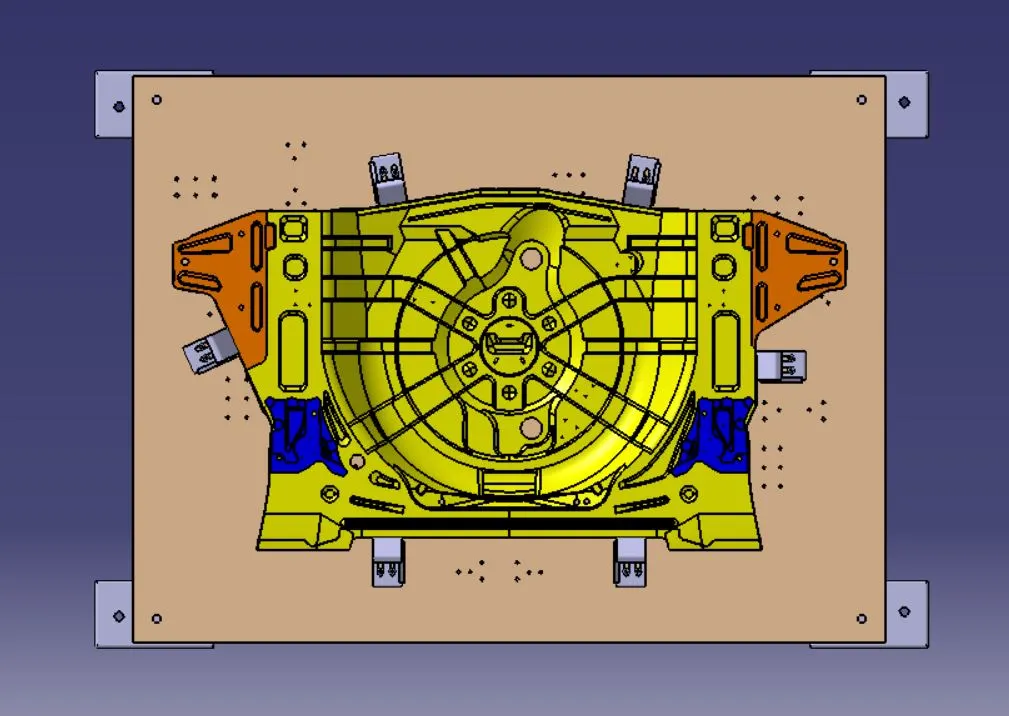
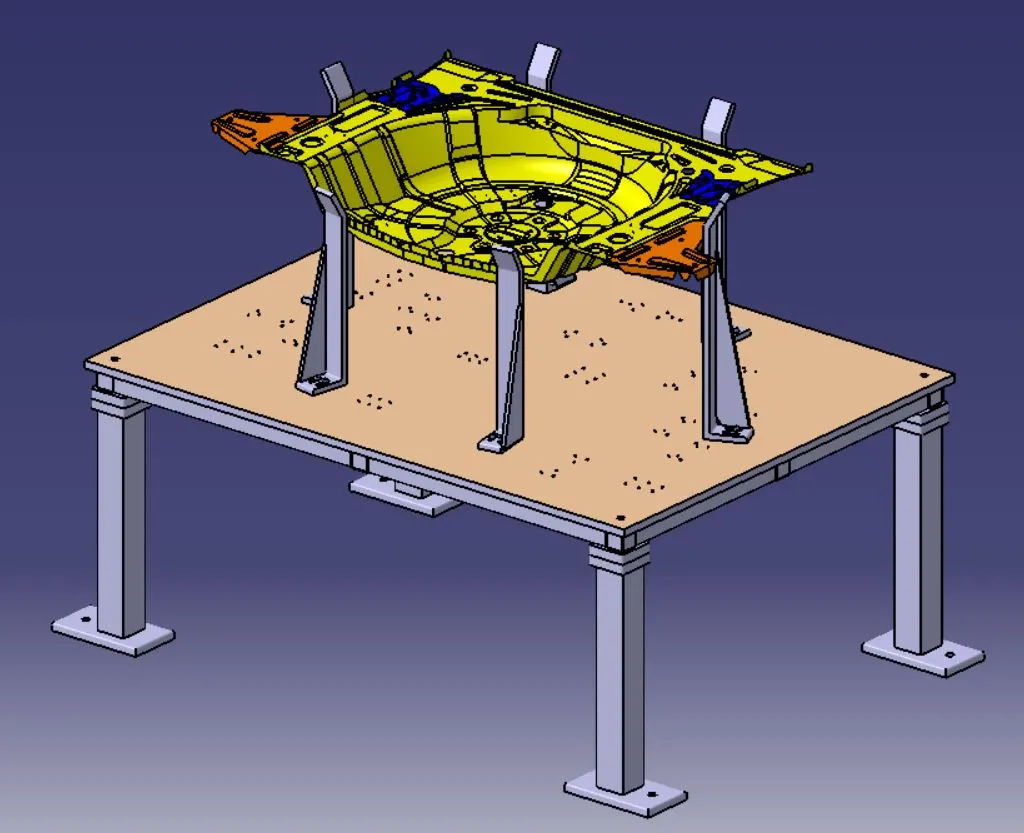
8 Rough Locator
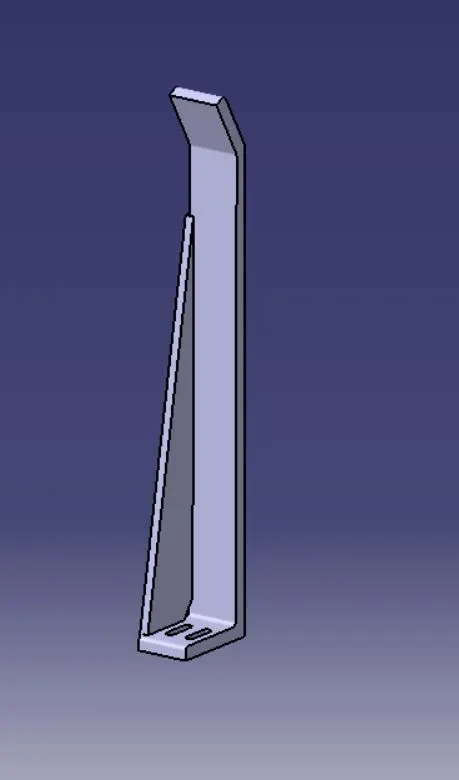
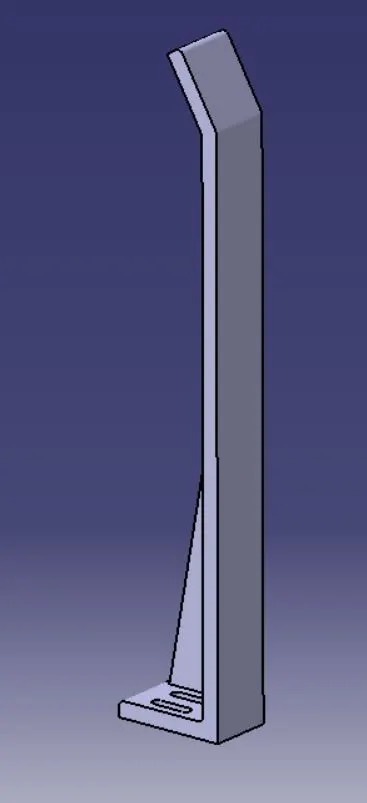
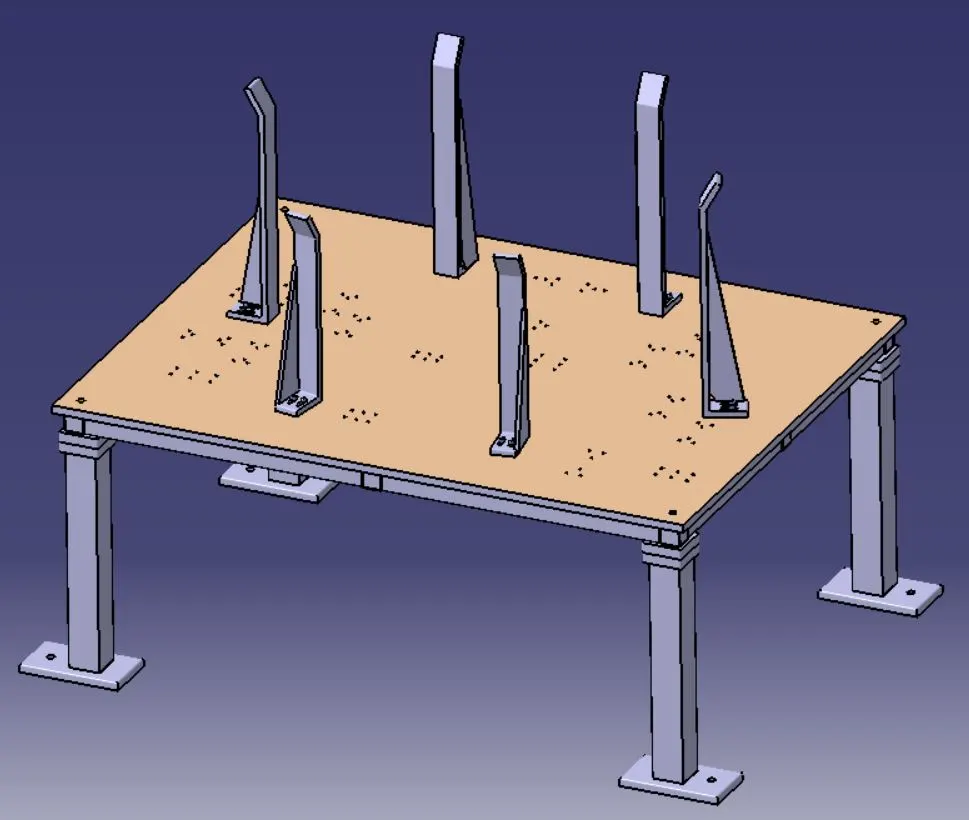
- Provide locator in 4 direction.
- Mention 0 mm gap between rough locator and panel.
- here I use 6 rough locators as shown below.
Final Render Image of fixture: