Week 6:- Clamp Unit & Pin-Clamp Unit Design Challenge
AIM :
To study the various design aspects regarding BIW fixtures.
OBJECTIVE :
To design 3 Different types of Swivel Clamp Units with Different Raisers, Blades, and Clamp Arms for the given Car Panel using the 3-2-1 principle.
To design a Pin-Clamp Unit for the given Car Panel.
3-2-1 principle
The 3-2-1 method is a work-holding principle where three pins are located on the 1st principle plane, i.e., either XY, YZ, ZX. Two pins are located on the 2nd plane perpendicular to the 1st plane, and at last, one pin on the plane is mutually perpendicular to the 1st and 2nd planes.
It represents the minimum requirement for the locating elements.
The locators along with the clams that hold the part in place, provide equilibrium for all the forces.
Stability is satisfactory if all three rest buttons are widely spaced and the resultant cutting force lies within the triangular area between the buttons.
If the resultant cutting force lies outside the triangular area then it generates a moment which in turn lifts are overturns the component.
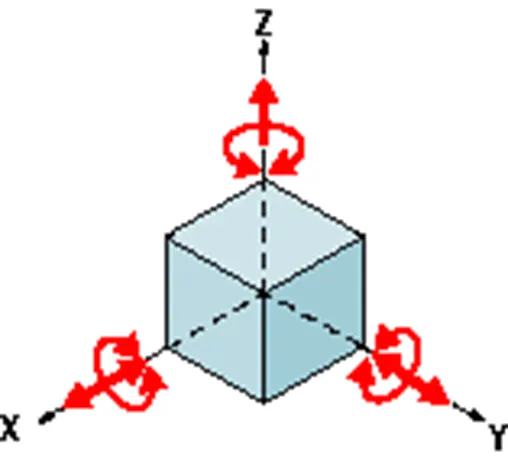
Locating Process in 3-2-1 method
We have two objectives when mounting a part in a fixture for machining
1. Accurately position the part at the desired coordinates.
2. Restrict all six degrees of freedom so the part cannot move.
A widely used method of accomplishing these two objectives uses the 3-2-1 principle, so-called because it entails three steps that employ three, then two, then one fixed points of known location. Since that adds up to six fixed points, it’s also known as the six-point method.
In the three steps of the 3-2-1 method, three mutually perpendicular planes, called datum planes, are introduced, one at each step. These three planes define the workpiece position, and together with opposing clamping forces fully constrain the part. Let’s take a look at the details of the 3-2-1 method
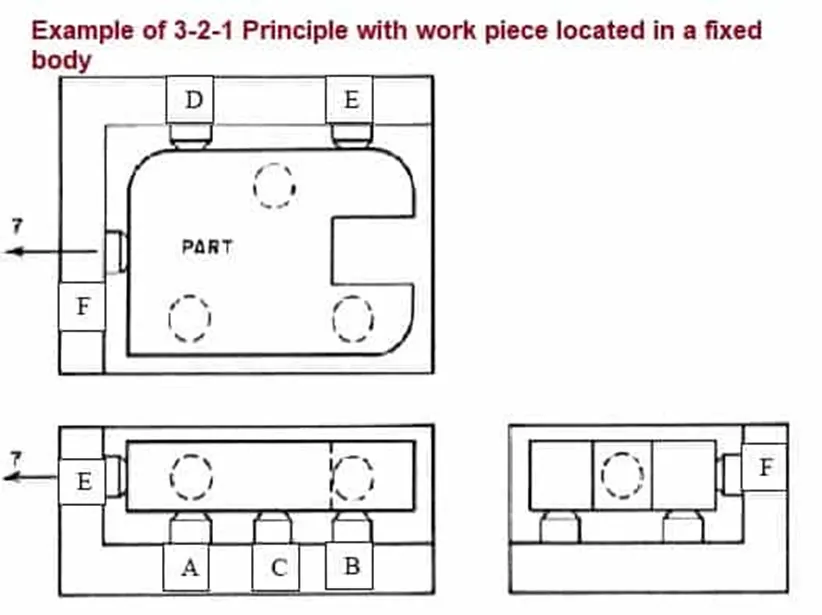
First Plane
Geometry tells us that three points are required to define a plane. This is the "3" in 3-2-1. So, three specific points are used to define the first plane. Fewer than three points cannot define a plane, and in the real world dimensional tolerances mean that four or more points will not be coplanar.
A real-world, less-than-ideally perfect part placed on four or more reference points will rest on only three of the points due to its less-than-perfect surface. Different parts may rest on different combinations of three points, resulting in variation between finished parts. A stool can be used to illustrate this concept.
A two-legged stool would certainly be unstable. A three-legged stool sits rock-solid. A four-legged stool is often found to rock. In the illustration, a three-dimensional part, represented by a cube, is placed on a datum plane defined by three support points.
The part’s six degrees of freedom have now been reduced to three. It can still move along the X or Y axes, and it can still be rotated about the Z axis. The part cannot move along the Z-axis because it is held against the plane by clamping force.
Second Plane
A second plane, if it is perpendicular to the first, can be defined by two points, the "2" in 3-2-1.
The part is now constrained to one degree of freedom, movement along the Y axis.
The part cannot move along the X or Z axes because it is held against the planes by clamping force.
Third Plane
A third plane, if it is perpendicular to both of the first two planes, can be defined by one point, the "1" in 3-2-1. The part is now entirely constrained. It cannot move along or rotate about the X, Y, or Z axes. (Remember that the part is held against each of the three planes by clamping force.
Supporting
The part is supported by "below" concerning the Z axis. (Introduction of the first reference plane.)
Gravity positions the part against the support locator.
Provide adjustable auxiliary support points as needed to prevent deflection.
Vertical location concerning the fixture is now established
The part is positioned horizontally, in the X-Y plane. (Introduction of the second and third reference planes.)
Holding
The part is clamped against fixed locators. Therefore, a known and unvarying position of the part is maintained concerning the X, Y, and Z axes.
One strap clamp or clamp arm will restrict the workpiece in three dimensions due to friction between the workpiece and clamp. However, friction alone may not be enough to prevent the workpiece from moving during machining.
Cutting forces will not move a properly supported and clamped part.
Summary of 3-2-1 principle
A workpiece will be completely confined when blanked against
3 points in one plane: The “3” in 3-2-1 refers to 3 locators (passive fixture elements) on the primary locating/datum surface.
2 points in another plane: The “2” in 3-2-1 refers to 2 locators on the secondary locating/datum surface.
1 point in a third plane: The “1” in 3-2-1 refers to 1 locator on the tertiary locating/datum surface.
Clamp Unit
A Clamp unit is a unit that is designed to calm or hold the car panel.
The various parts of a Clamp unit are as follows,
Clamp Arm
Clamp Cylinder
Finger
Rest
Locators
Shims
Plate
Riser
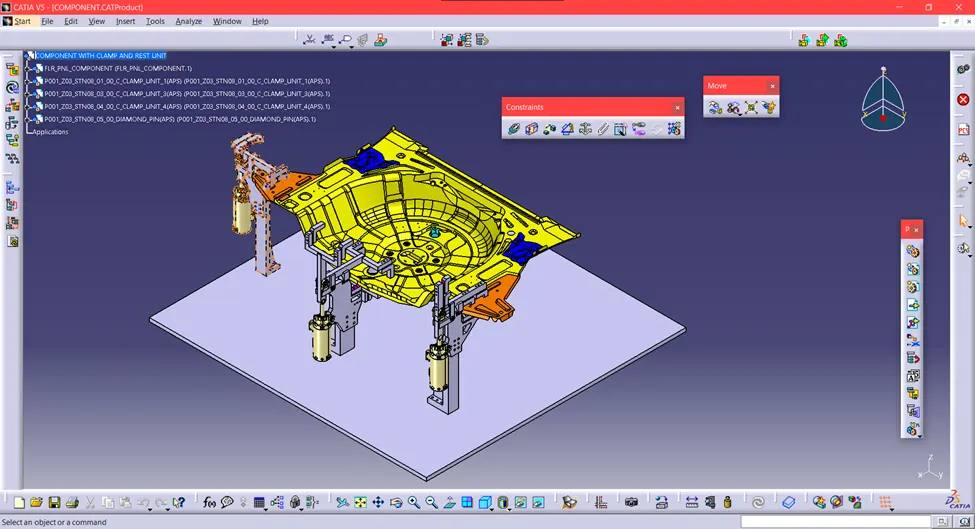
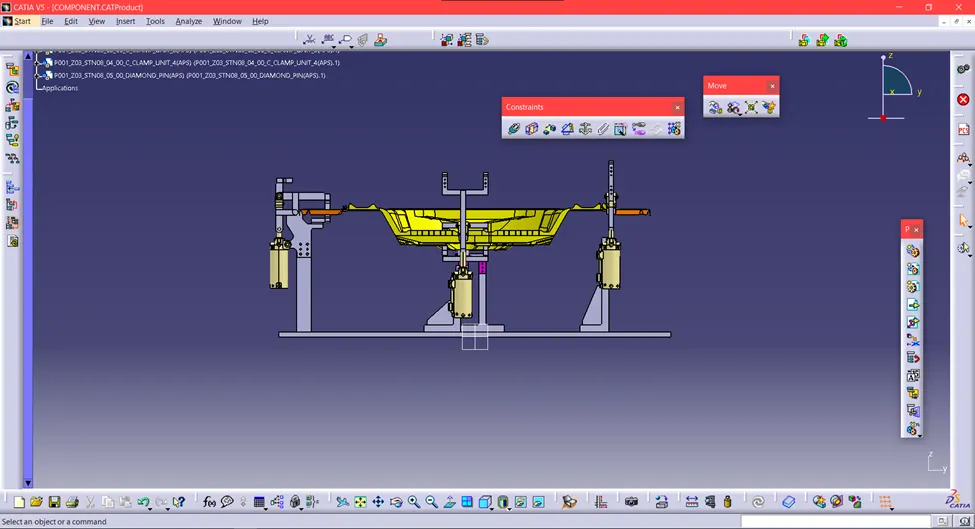
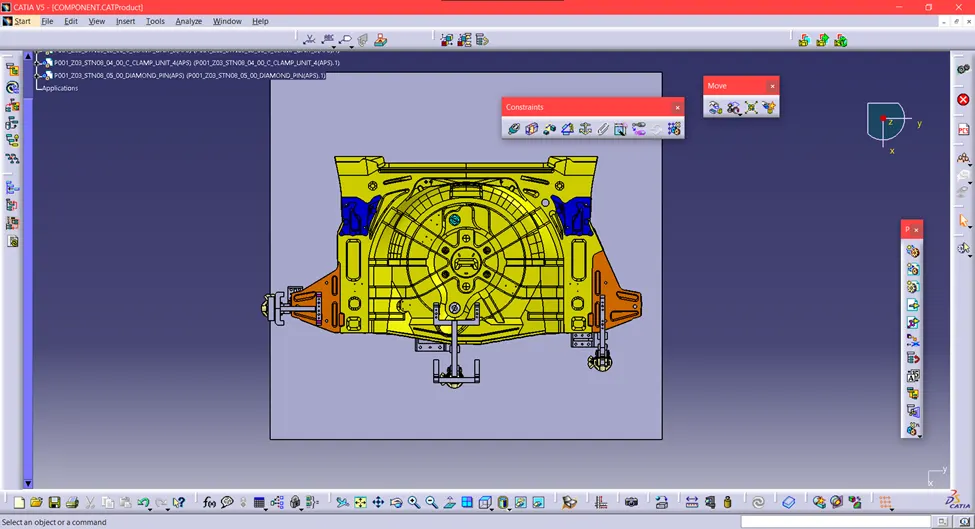
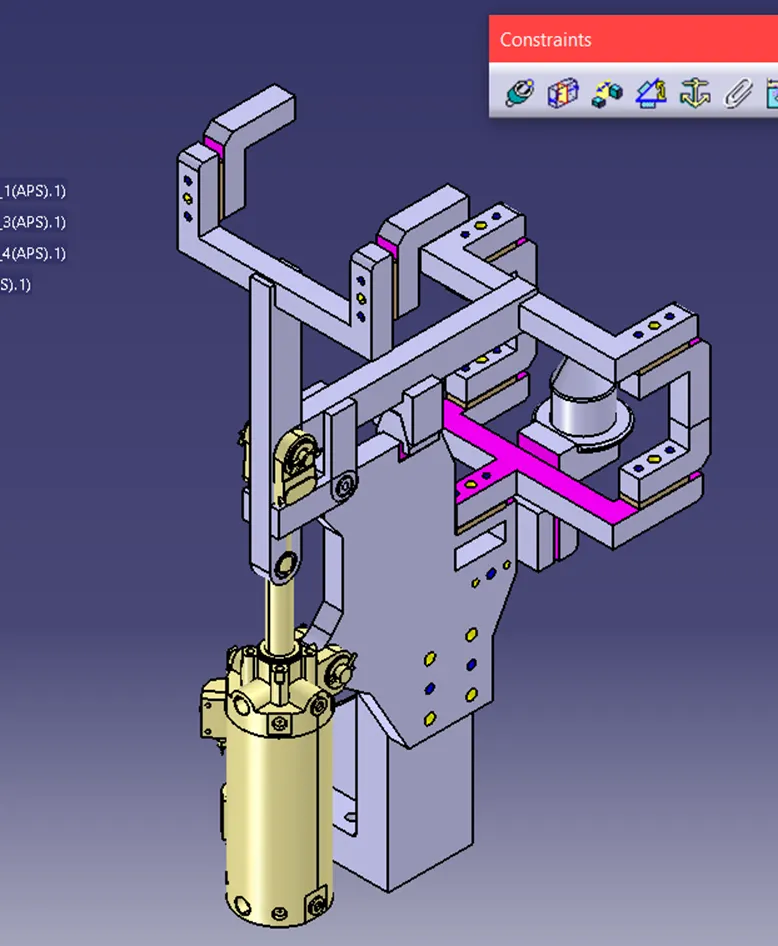
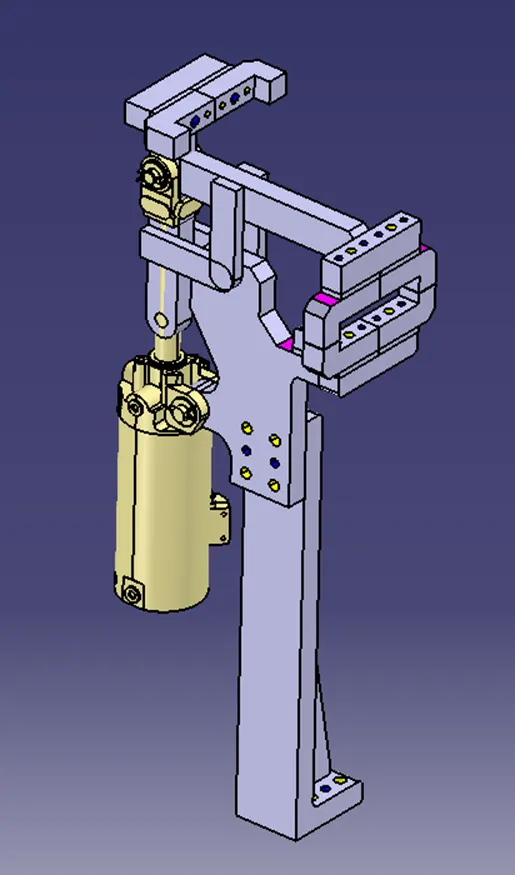
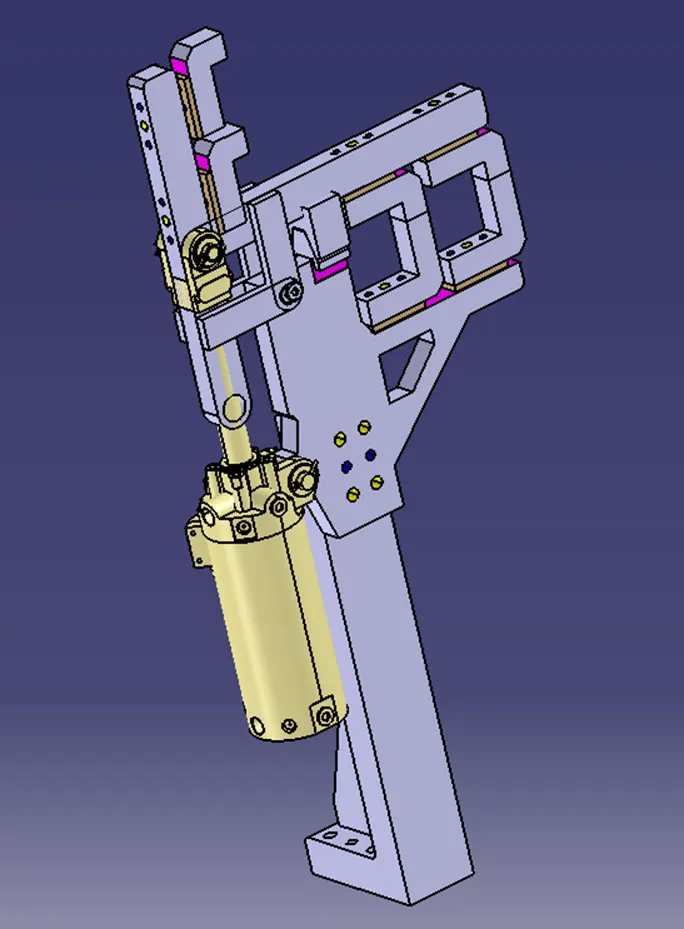
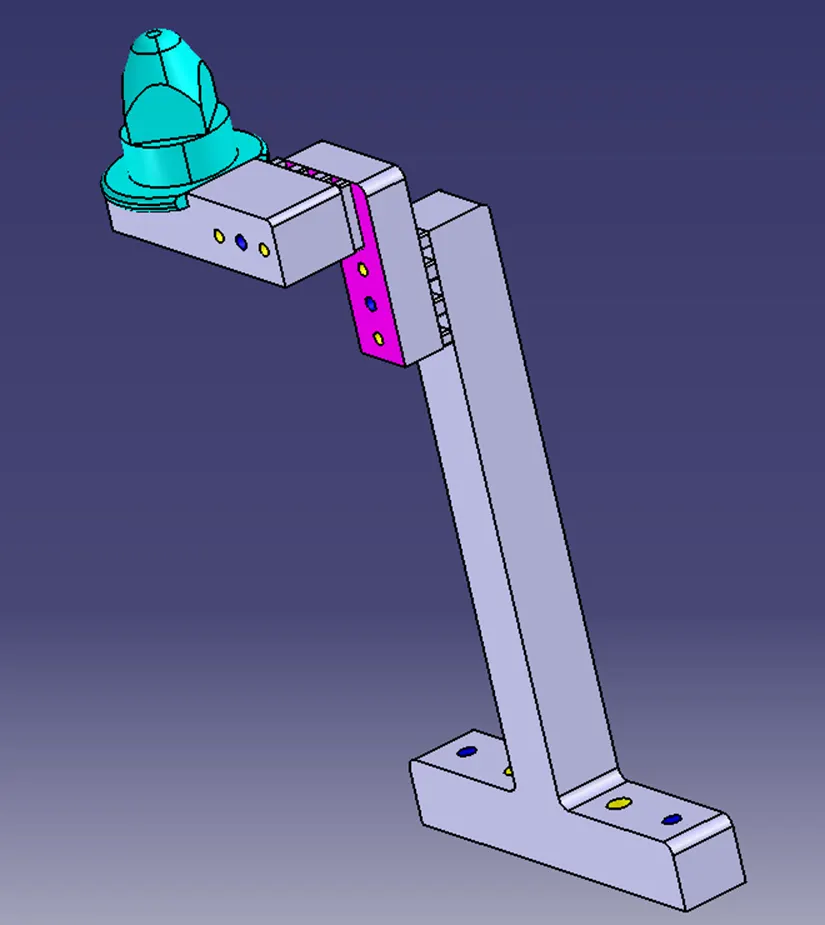
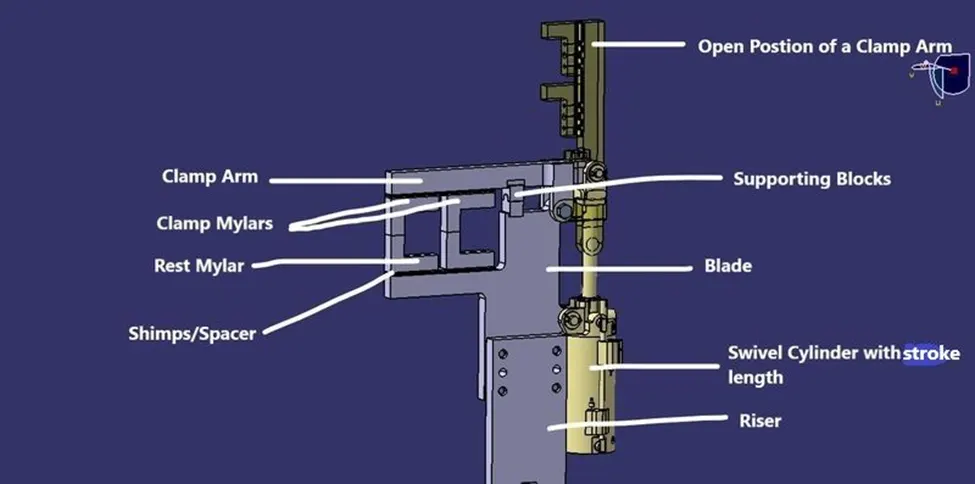
FACTORS SHOULD BE CONSIDERED WHILE DESIGNING THE CLAMP UNIT:
Should use standard part as possible i.e.NAAMS standard.
There should be adequate space between the cylinder and other parts like the riser, and car panel. Because the cylinder moves or swings while opening and closing.
A pin clamp unit is used where two panels or components are located and clamp for welding.
clamp is made in such a way that it clamps two car panels at once.
every clamp mylar/NC block should have a rest mylar or unit.
clamp unit has shims in only one direction.
ALL parts should snap and butt properly to each other.
Make sure that parts of the clamp unit are 10 -12 mm away from the car panel.
The design tree should structured in a way that makes part on the top and follows the standard part.
The position of the clevis joint pin will be in one line.
Avoid any clash, It will not raise issues at assembly.
product should designed in such a way that it will be easy to make, assemble, and quality check.
we should preferably use quick-acting clamps. The clamping method must not damage our workpiece.
the clamp should open so that the clamp arm moves away from the operator.
There must be adequate clearance for loading and unloading so that the process becomes fast and easy. The variation in size must be accepted.
Avoid sharp edges and corners, they can harm the operator and cause to serious injury Provide chamfer or fillet to the corner.