Week 3 Verification of Weld Joints
Aim : To verify weld joints using static structural analysis
Conclusion :
1) To simulate three different types of welding using three different weld materials
2) To fine out the directional deformation and equivalent strain experienced by the setup
3) To identify the weld joint that experiences the highest equivalent stress in each case and compare the results for all three cases
Introduction :
Welding is a very commonly used permanent joining process. Recent years we have accomplished mngreat advancement in welding technology, it has secured a prominent place in manufacturing machine components. Compared to other type of joints, the welded joint has higher efficiency. An efficiency > 95 % is easily possible. Since the added materialis minimum, the joint has lighter weight. Welded joints have smooth appearances. Due to flexibility in the welding procedure, alteration and addition are possible. Forming a joint in difficult locations is possible through welding.
The advantages have made welding suitable for joining components in various machines and structures. Some typically welded machine components are listed below.
Pressure vessels,structures.
2. Flanges welded to shafts and axles.
3. Crank shafts
4. Heavy hydraulic turbine shafts
5. Large gears, pulleys, flywheels
6 Gear housing
7. Machine frames and bases
8. Housing and mill-stands
Procedure :
1) To verify welds in the setup, we use static structural tool in the analysis system tool box to define the geometry and other input parameters for the same.
First we open spaceclaim to identify and rectify the errors in the geometry. In the below geometry we can see the welds are
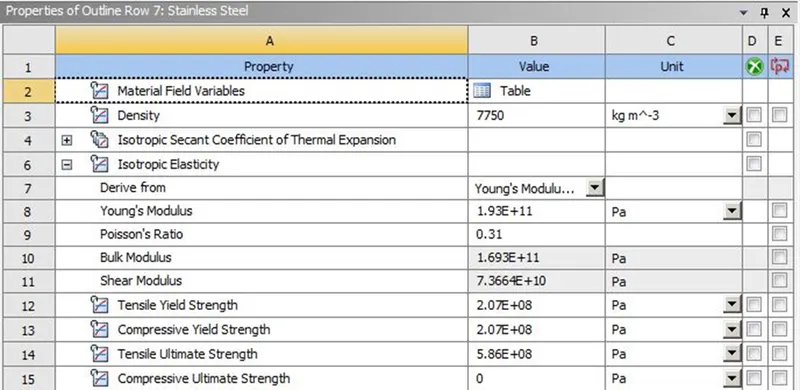
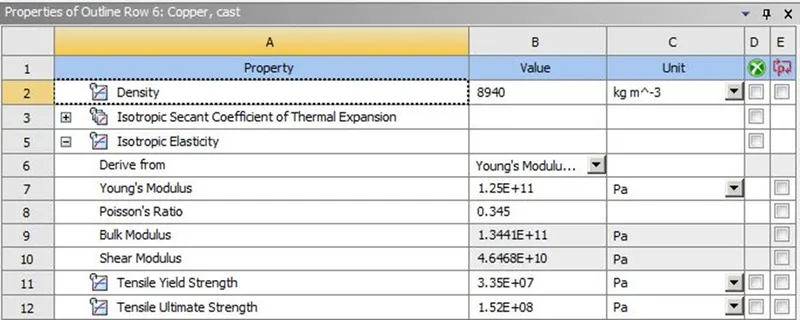
2) In the engineering data we input the material and its properties. In this case we are using three different types of materials and its properties are shown below.
Case 1 :
In this case, the material of the plates must stainless steel. Use Stainless steel for both weldments and plates. No need to add flux to the weldments.
Case 2:
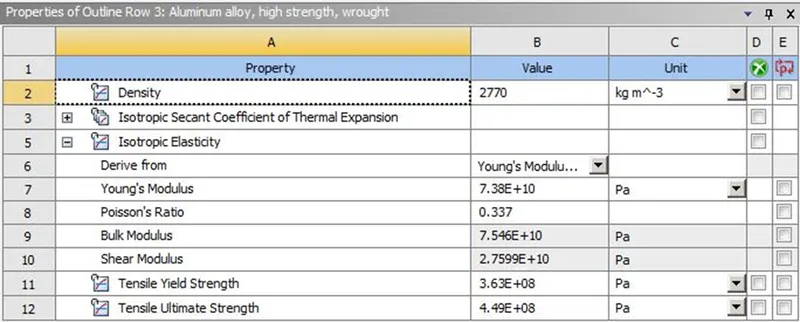
Aluminium Alloy:The material to be chosen for this case is Aluminium alloy(high strength, wrought). [Plate material to be used is stainless steel]
Case 3:
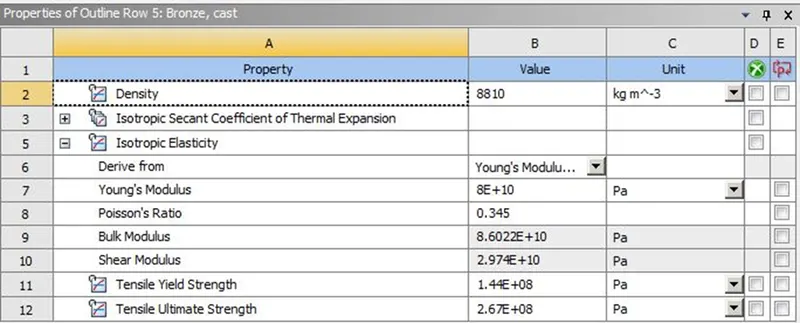
Bronze: In order to simulate "Brazing", should be using bronze as the weld material. Assign Stainless Steel to both plates and Copper to the "Ribs".
3) Input the given weld geometry from the geometry tab and naming them.
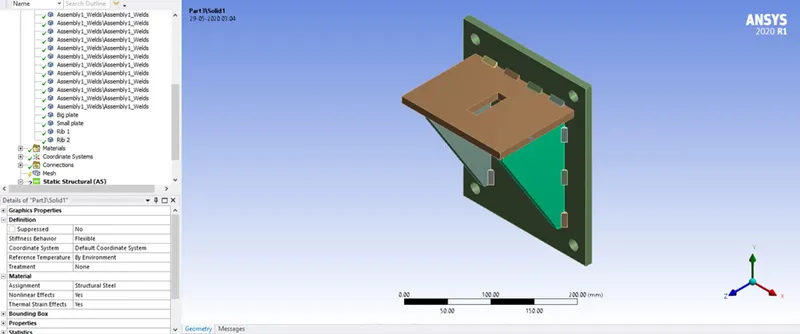
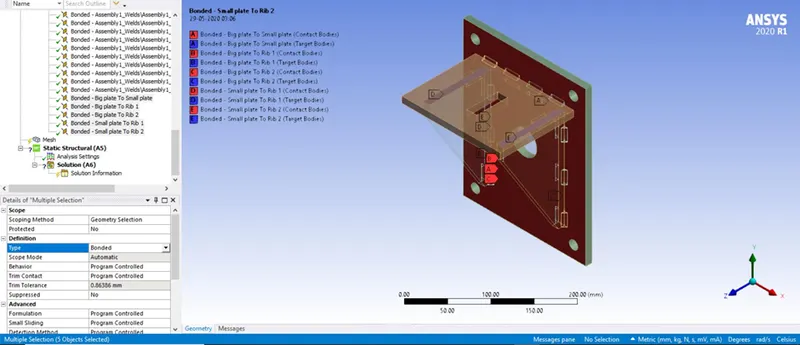
4) In connection, we have to define the contact faces of the weld geometry by selecting and deselecting as contact or target bodies. In contacts under connection tab we define the type of contact as frictional contact with coefficient of friction as 0.3 for connection between ribs and plates. Connection between the plates and weld joints are kept as bonded.
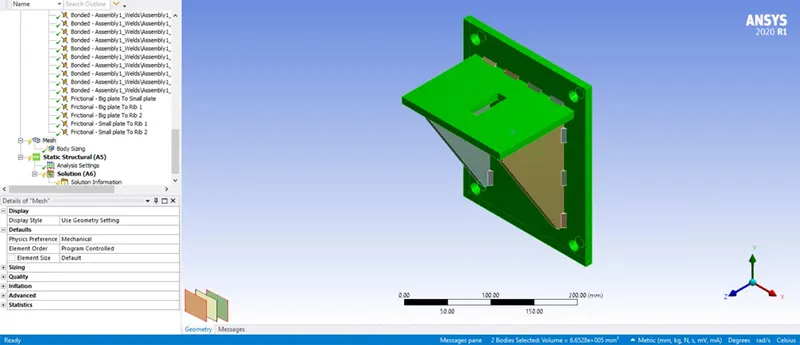
5) By opening the modelling the tab, we mesh the geometry with element size as default. Generating the mesh thereafter by right clicking on the Mesh icon. Body sizing under mesh tab is used to refine the mesh to 7mm for two plates where contacts are present.
Body sizing of 7mm mesh
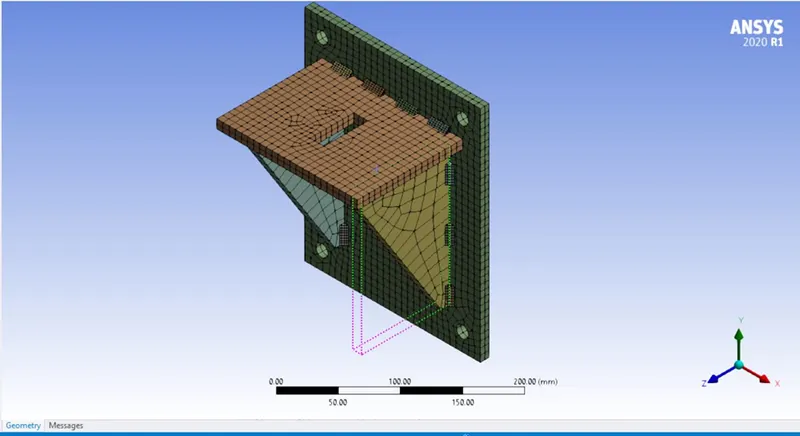
6) We open analysis setting where we define step control settings and input the parameters as needed.
Defining Fixed support with one step by selecting the faces
Force applied in the Y direction of 15000N.
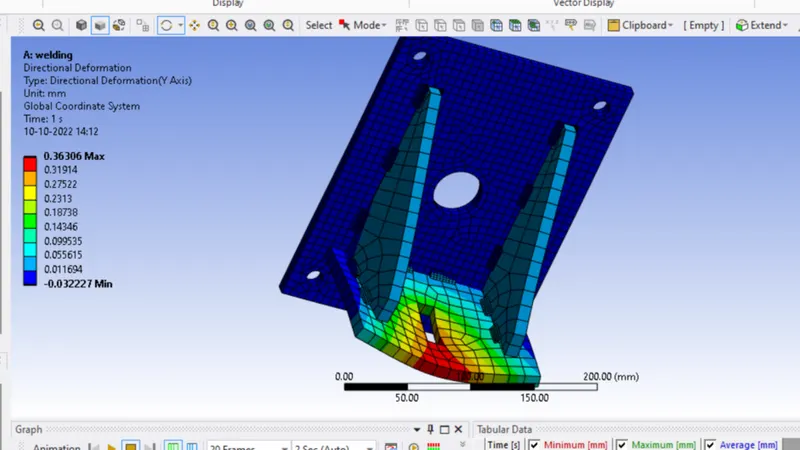
For Case 1 :
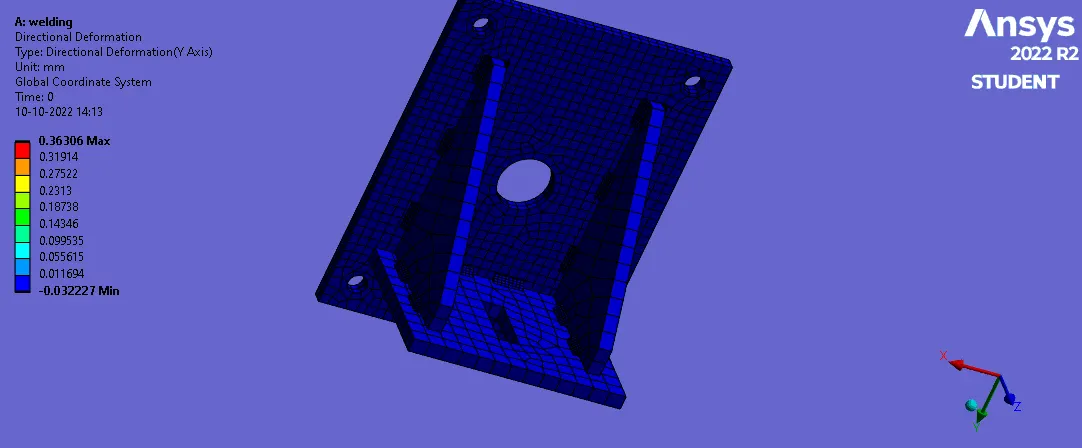
Deformation.
Directional deformation (Y-axis)
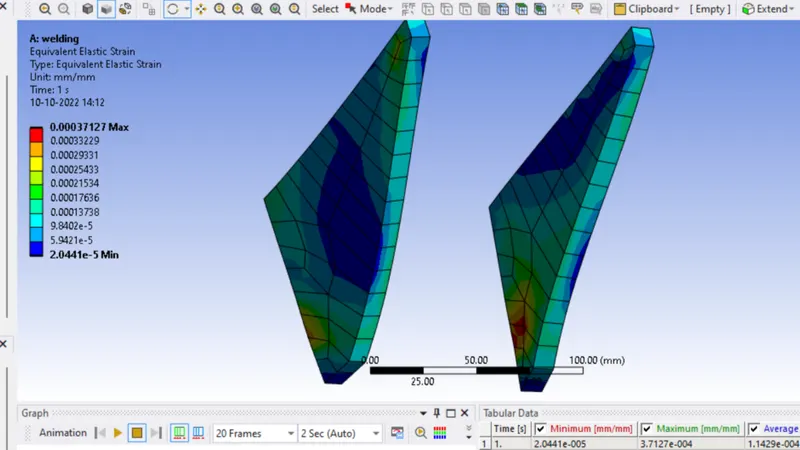
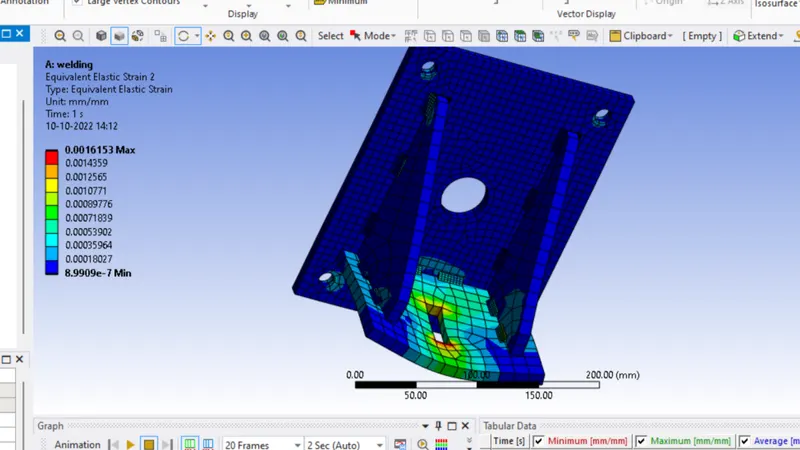
Equivalent strain.
In ribs
Body
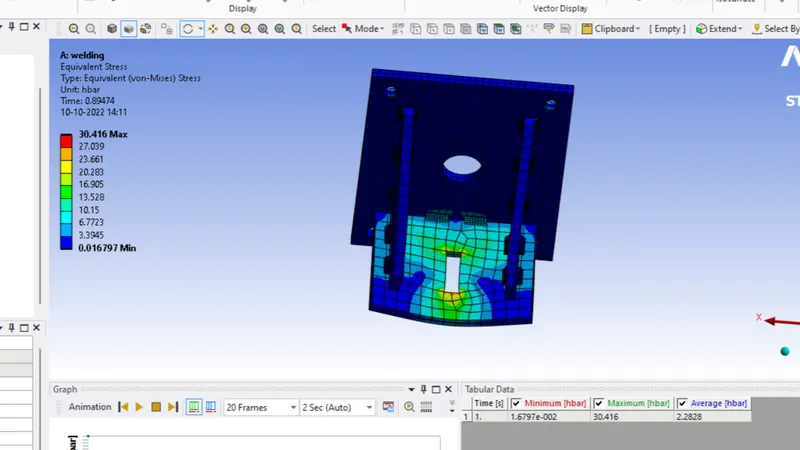
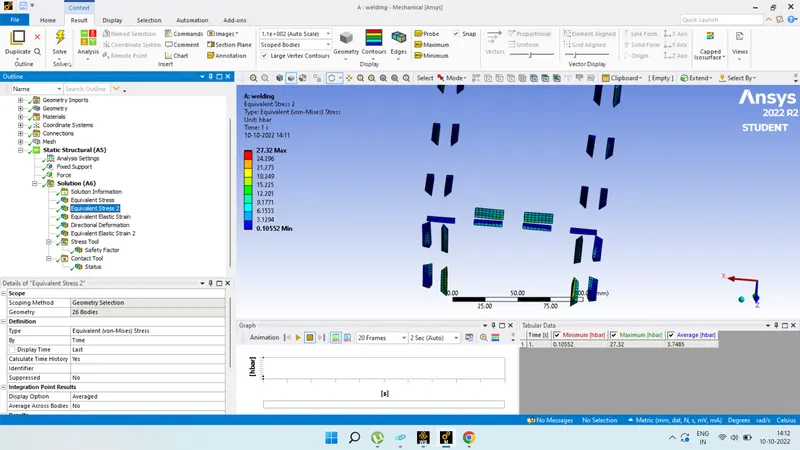
Equivalent stress
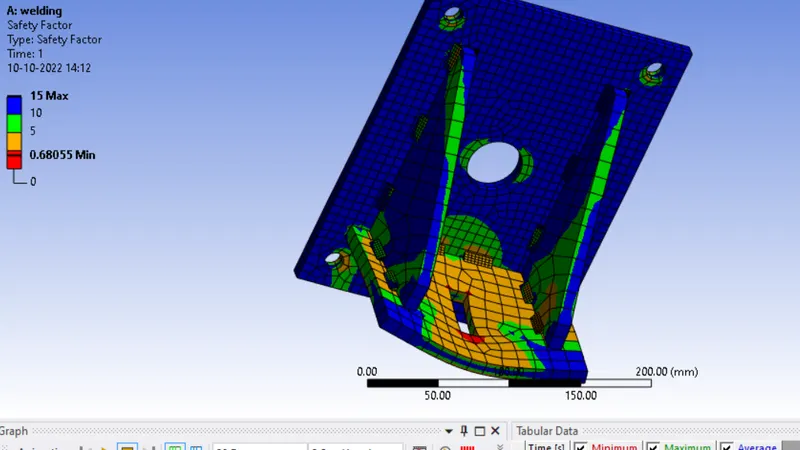
Saftey factor
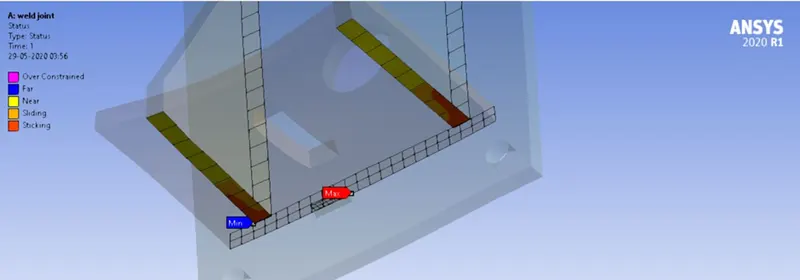
Contact
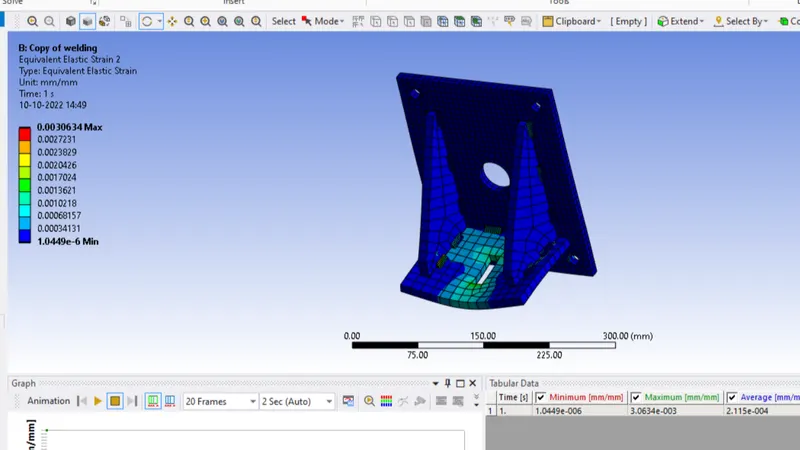
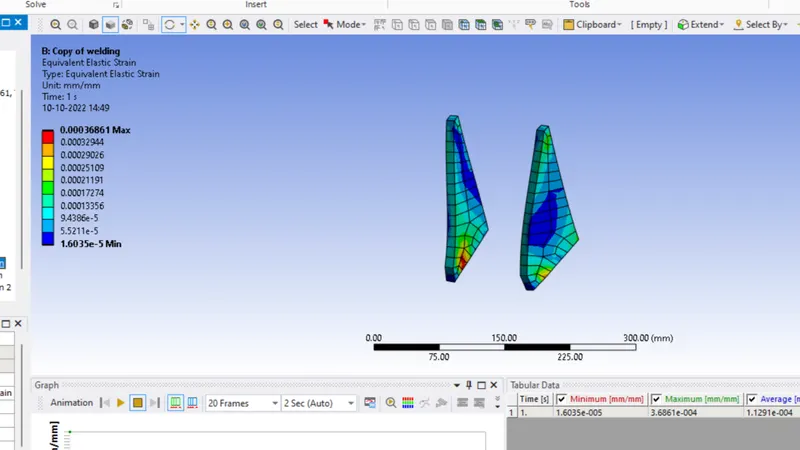
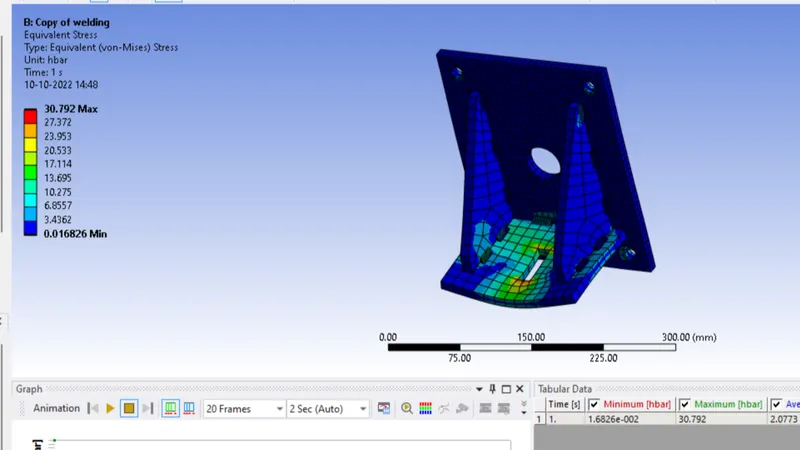
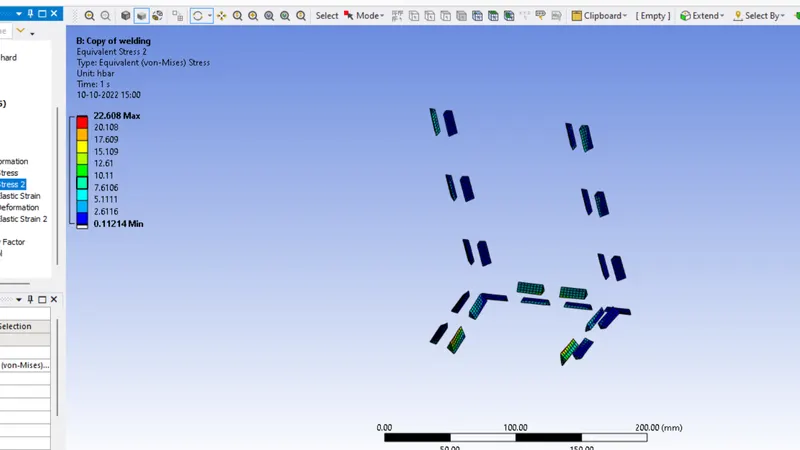
Case 2. Aluminium Alloy:The material to be chosen for this case is Aluminium alloy(high strength, wrought). [Plate material to be used is stainless steel]
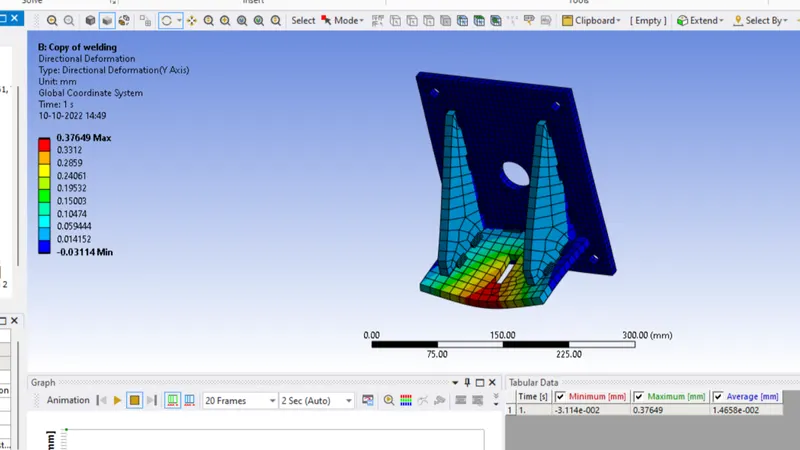
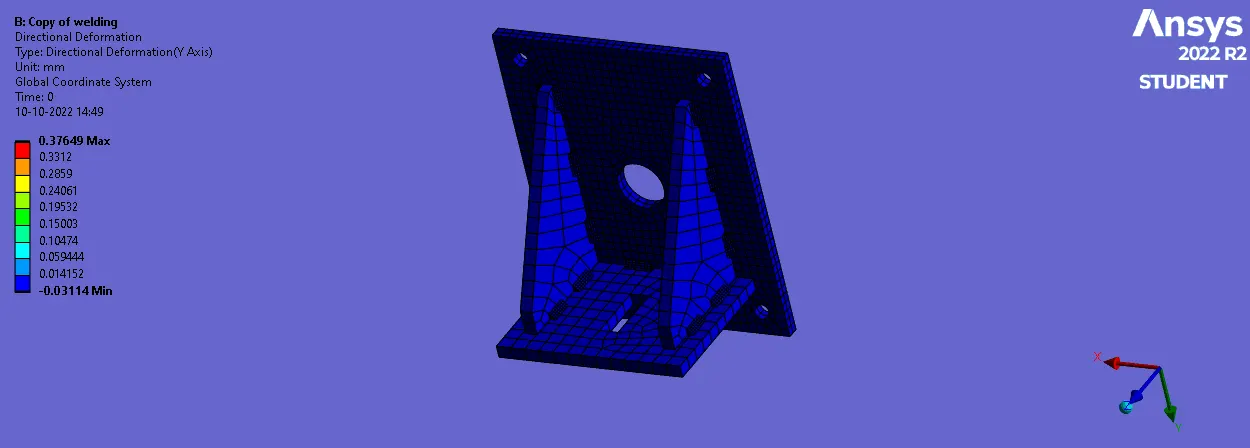
Deformation in y direction
Starin
Equivalent stress
Saftey factor
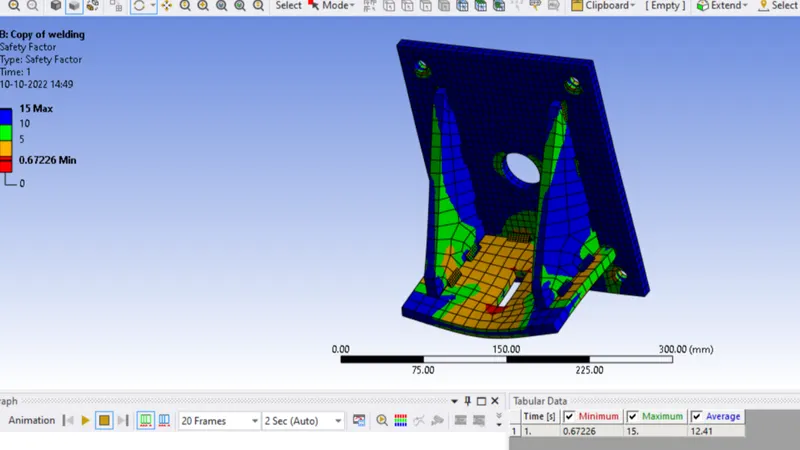
Contact
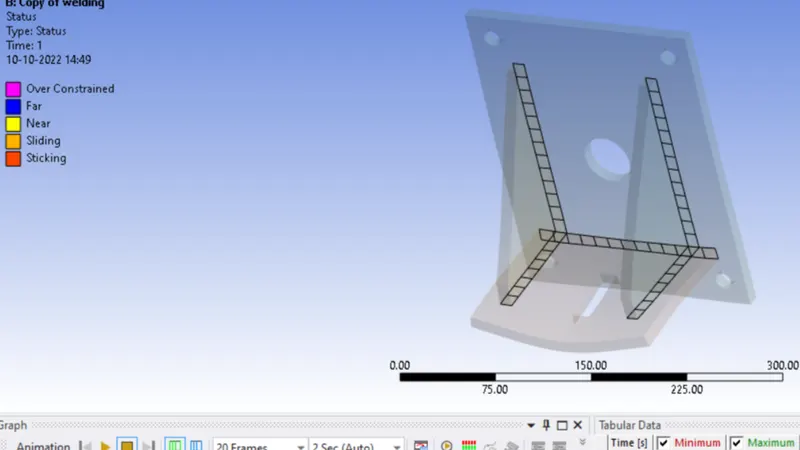
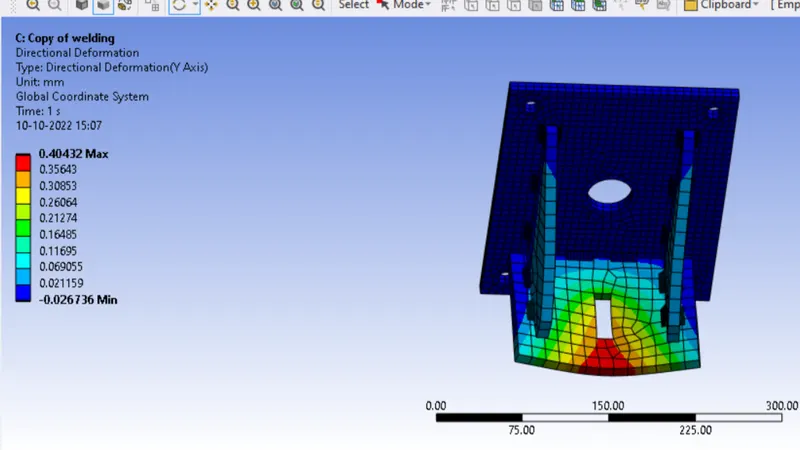
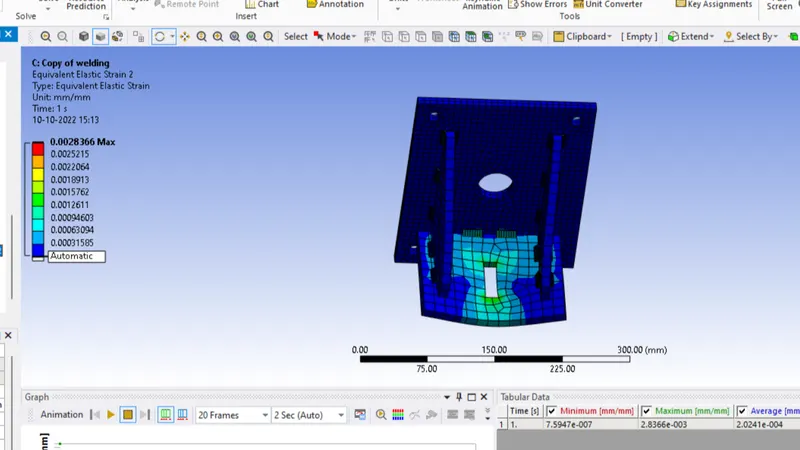
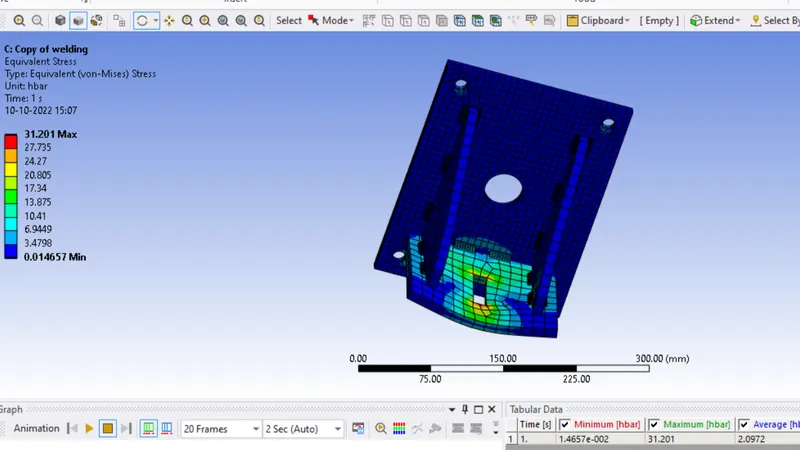
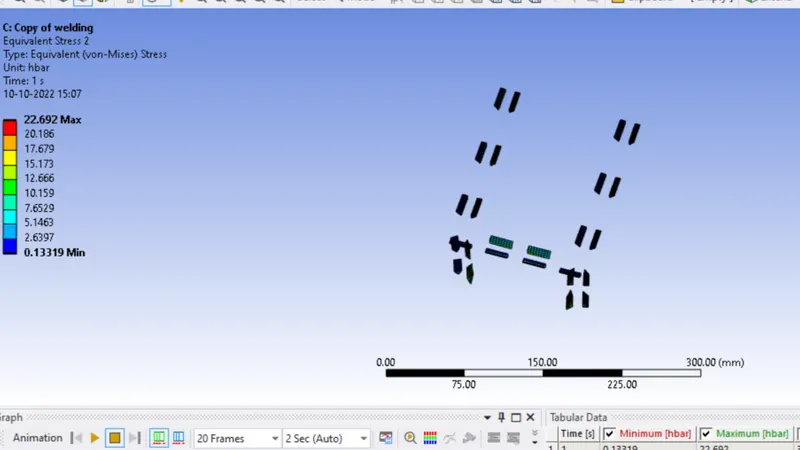
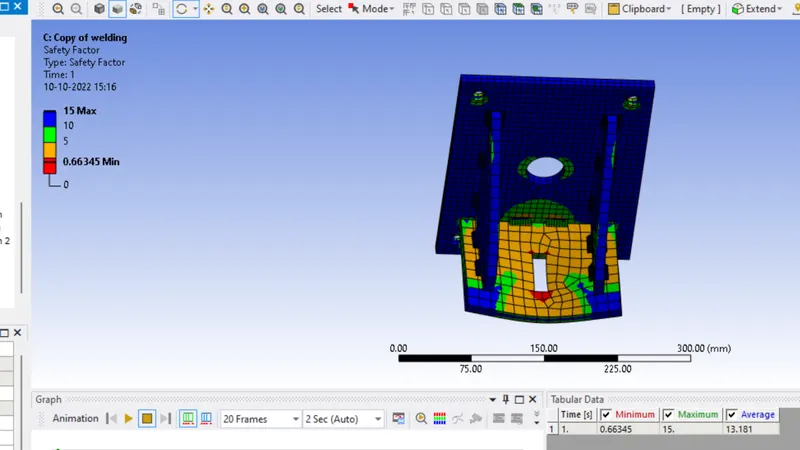
Case 3.Bronze: In order to simulate "Brazing", you should be using bronze as the weld material. Assign Stainless Steel to both plates and Copper to the "Ribs".
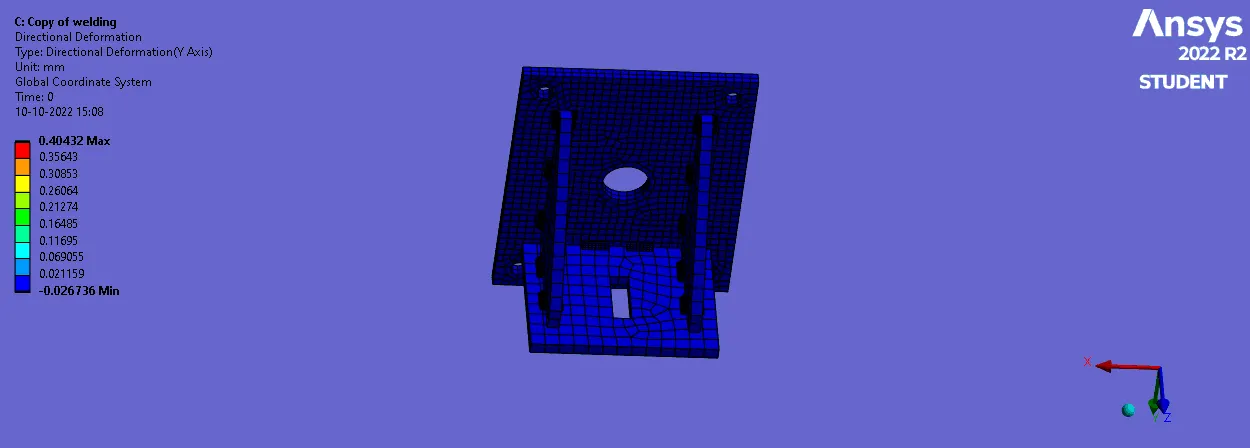
Directional deformation.
Strain body and ribs
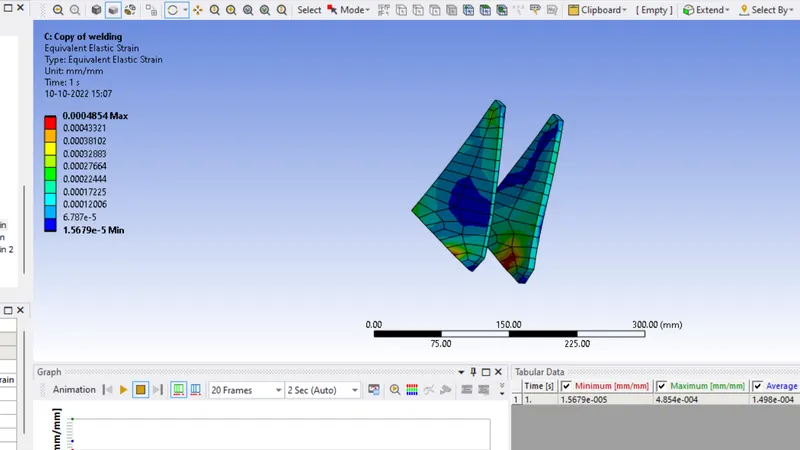
Stress
Saftey factor
Contact
Animattionn
Deformation
Case 1
case 2
case 3
| MATERIAL | EQUIVALENT STRESS (MPa) | DIRECTIONAL DEFORMATION (Y-Axis) (mm) | STRAIN | RIB STRAIN | EQUIVALENT STRESS AT WELDMENTS (MPa) |
| Stainless Steel |
MAX: 304.16 MIN: 0.16 |
MAX: 0.3630 MIN: -0.0322 |
MAX: 0.0016 MIN: 8.99e-7 |
MAX: 0.00037 MIN: 2.04e-5 |
MAX:273.2 MIN: 65.0 |
| Aluminum |
MAX: 307.9 MIN: 0.16 |
MAX: 0.376 MIN: -0.0311 |
MAX: 0.00306 MIN: 1.0159e-6 |
MAX: 0.00036056 MIN: 1.6043e-5 |
MAX: 226.08 MIN:0.112 |
| Bronze |
MAX: 312.01 MIN: 0.1467 |
MAX: 0.404 MIN: -0.026 |
MAX: 0.002813 MIN: 2.1863e-7 |
MAX: 0.0004868 MIN: 1.56173e-5 |
MAX: 226.92 MIN: 0.13319 |
- The above tabular data shows the variations in the equivalent stress and directional deformation of various material such as Stainless Steel, Aluminium and Bronze. Aluminium material experiences more stress and directional deformation where compared with case-1 and case-3.
Conclusion:
- From the above result we can conclude that the equivalent stress and maximum directional deformation takes place in Case-2. The maximum deformation takes place in case-2 because in this case the material is Aluminium
- From case-1, the ribs, plates and weldments are assigned with same material as stainless steel and experiences more stress at weldments due to high yield strength of material as well as in case-2, the stress at weldment is high when compared with case-3.
- The usual causes of material failure are incorrect materials selection, incorrect processing, incorrect manufacturing procedures, inadequate design or incorrect use. Fracture is the separation of a body into two or more pieces as a result of an imposed stress. Here the aluminum material will not fail as the FOS of this material is 1.22 when compared with other two.
- FOS= YIELD STRESS/WORKING STRESS,
FOS of aluminium = 363/296.69= 1.22.
- Grid dependency test will be important for selecting the suitable mesh size.