Week 3:- BiW Fixture Design Methodologies Challenges
Q) What is design methodology?
Ans: Design Methodology is nothing but the steps followed during the concept designing of fixture design. Below are the steps followed during the design methodology.
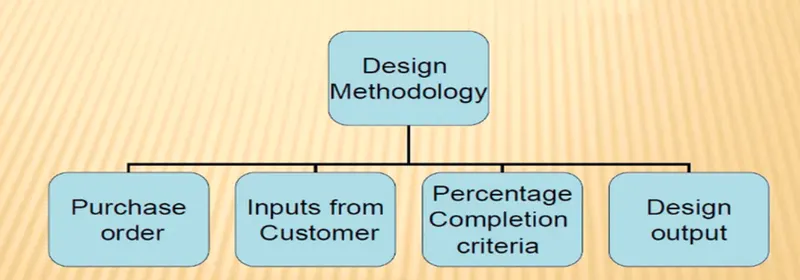
Purchase Order: Purchase order basically confirmation from customer side that we are ready to start work. It’s is the standard document buyer giving to the seller for further process .it will include how much qty, what is the cost of the product, and when delivery require etc with all those information.
Input from customer: Input from customer are the major inputs that we get from customer, how do we study those input what kind of information and get out of those input, these are the criteria that we mentioned in this particular input from the customer.
Percentage completion criteria: It consists planning of completion of total project. how many days the project will take to complete. It is followed in designing stage and dispatch stage of the welding fixture. It ensures that how much task that we have decided to complete within the stipulated time is complete or not and how much of its rest to complete and whether it’s going to be complete or not in given time.
Design Output: In BIW fixture design or any industry. We don’t only just design a particular component and just give the CAD file to the customer, you have to give a lot of documents like 3D,2D document, which is the detailing part and as well as other factors well like BOM, BOM bill material and other document as well about this particular component and their standard all has to be submitted to the customer.
Q) What are the inputs required from the customer to start designing a fixture?
Ans: The following are the inputs required from the customer to start the fixture design work.
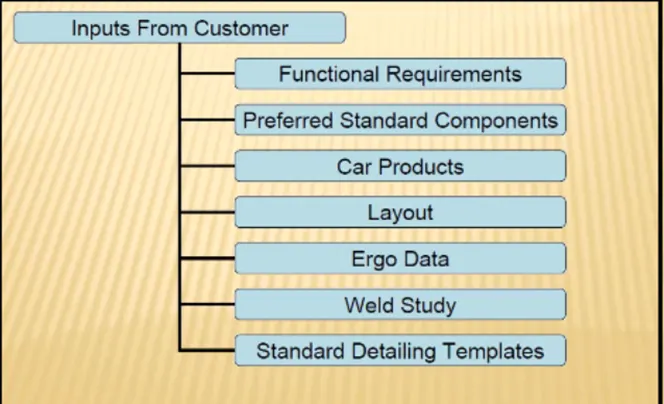
Functional Requirement: In functional design requirement this is basically what kind of functional that particular design going to have for example welding, Gluing, riveting fasting this kind of information will be given us.
Preferred Standard Components: We have to consider as much as possible standard component in our design because it will save our money as well as time also. Some time some of the component customer already have so we no need to buy one more time. For different company using different standard for their component. If we are using standard component then we can easily buy standard component from outside of the market as per our requirement.
- Standard like ABB, NAAMS, FAUNC, FESTO, TUNKERS
- Standard parts like riser L-block, retainer, pins many other companies actually manufacture this
- Some component like clamp, cylinder, slider, switches, sensors.
- Weld guns, Tip Dressers, Tool changers
Car product: Car product like 3D files, read files as well as to learn and to study what kind of geometrical tolerance and what kind of PLP points (Principle locating points) where we can fix those pinion edge and or the clamping edge and then putting position.
Layout: Layout provided information about flow of parts station pitch, robot station and accessors like tool changers, Tip dressers, Platform height, sub assembly link and loading /unloading sequences.
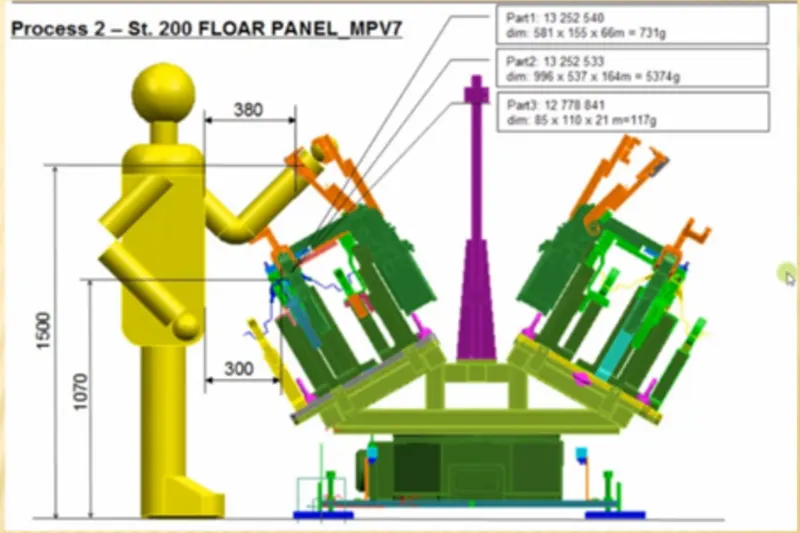
Ergo Data: Ergo data is basically involved well manual operator are involved and every company has different types of standards for aggregate data, so we will be getting that particular input from the customer so these are the standard that we follow so this kind of Ergo data we get from customer. It provided data regarding loading height, working safety zone of the operator etc as per standard that company follow.
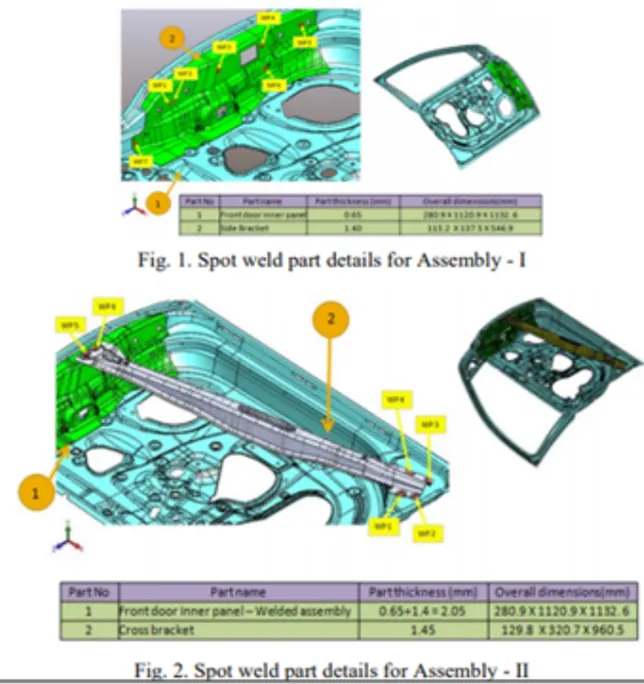
Weld study: Weld study means a study of the particular gun that we are going to use for welding and where are going to weld .so if we are doing spot welding what kind of spot welding, we are going to do a number of welding to the particular component.
Standard Detailing Template: Standard detailing template means every company has different type of standard, so they will give us detailing template about how to detail the particular component and dimension.
Q) what is the input we get from Car Products?
Ans: Car product like 3D files, read files as well as to learn and to study what kind of geometrical tolerance and what kind of PLP points (Principle locating points) where we can fix those pinion edge and or the clamping edge and then putting position
Car product include:
- GD&T
- Part list
- CAD files of car part
- Clamp plan
- Product assembly process sheet
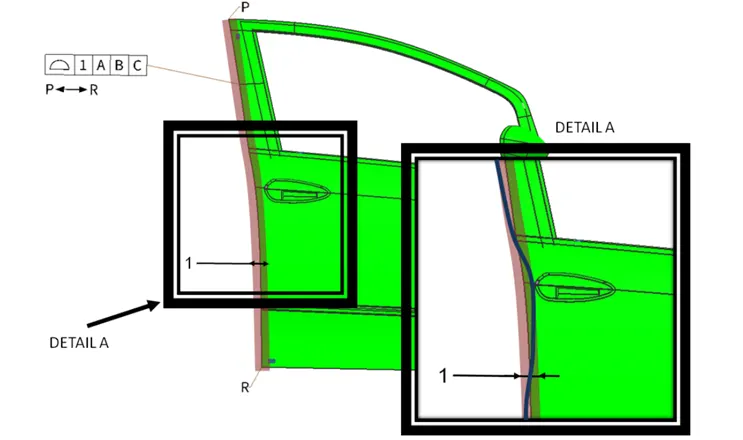
GD&T : GD&T Provides information of locating pins ,rest clamp ,dumps and slide information of each station. Sequence of opening of clamps, dumps and slide stroke information.
Part list: We are going to list down all the part name, part number, thickness of the part and their thickness which are going to add on assembly of the product. One assembly their lot of part of going that will be different part name. if some item we are going used the part, then serial going to be change.
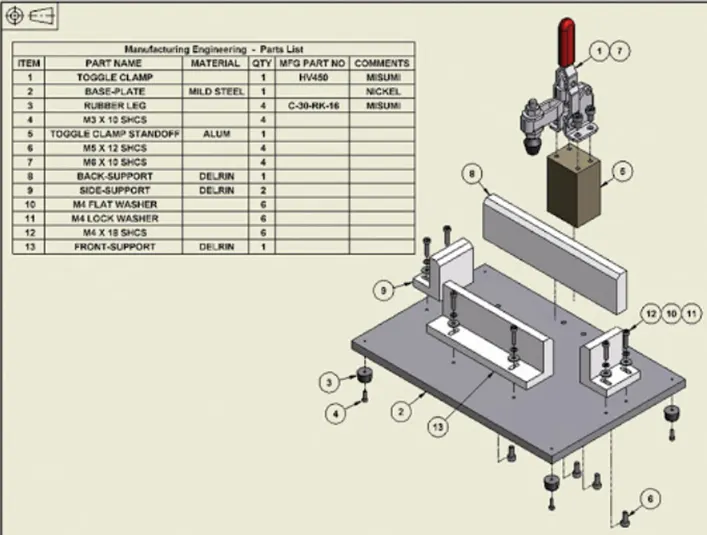
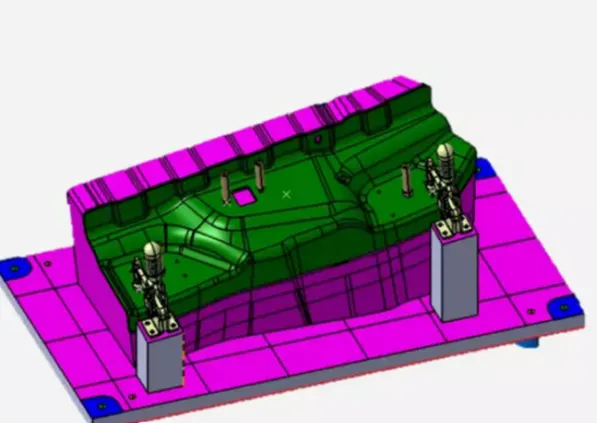
CAD file of the car parts: 3D file of that car product requires from customer. The 3D model file of the car part is given from the customer to study on it. The car part is designed by using 3D modelling software. From this we can get some conceptual idea of the designing of fixture.
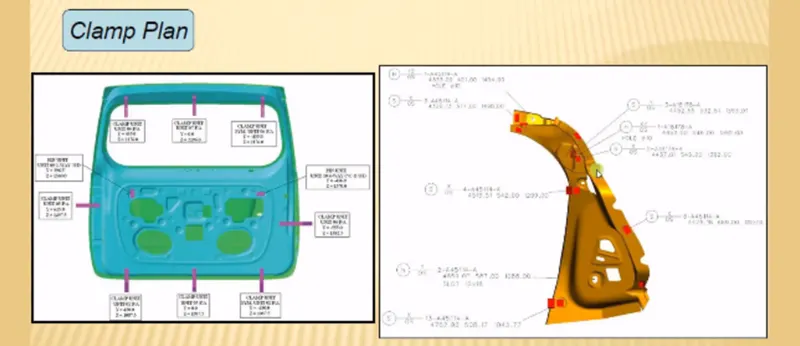
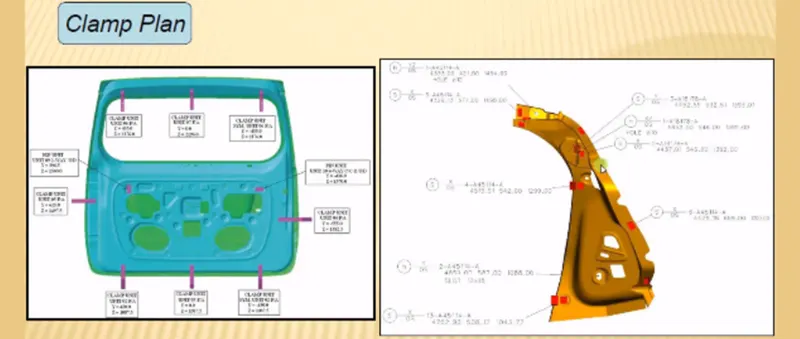
Clamp Plan: Clamp plan is a very important input that we get in the car products is where exactly we can place those clamping units are the particular Pin Units. We should not change the position of the particular clamp or the pin which is given in these data. We can change our design a little bit here or there but we should not change the input design data about the clamp position or the pin position.
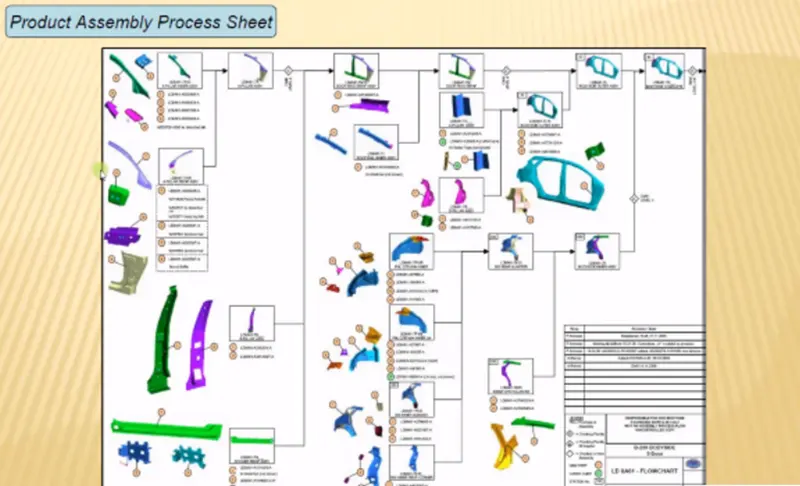
Product Assembly Process sheet: It’s provided the details process of the assembly, from initial level to finish level of the assembly. It will provide the standard how you have to perform assembly and which part we have assemble.
Q) What is the Clamp Plan?
Ans: Clamp plan is very important input that we get in the car products is where exactly we can place those clamping units are the particular pin units.
- We should not change the position of the particular clamps or the pin which is given in these data
- We can change our design a little bit here or there but we should not change the input design data about the clamp position or the pin position
- In the clamp plan there is a clamp unit, Pin unit and it’s more detailed .it also gives exact location of Y and Z coordinates designing as well you can just input these coordinates and you can start designing from there.
- If the three coordinates whole diameter and everything are already gives to design the entire future design phase .it happens that another thought position also gives very close to the clamp or the clamp location .so always ask whether you have changed the clamp position.
- You should never change the vent position or the clamp position without asking it so always be vary about these situations so the tool might get damage for that itself need to clarity once again before doing any changes in the clamps
Q) What is the purpose of the layout?
Ans: Plant layout is plan of an optimum arrangement of facilities including personnel, operating equipment, storage space material handling equipment and all other supporting services along with the design of best structure to contain all these facilities an overall objective of plant layout is to design a physical arrangement that meets the required output quality and quantity most economically.
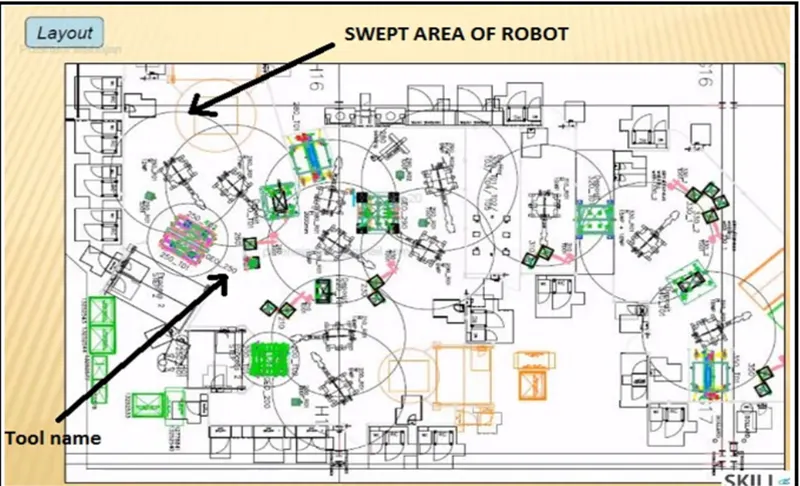
It shows all the objects of manufacturing line like robots, fixture, racks etc, and also shows the reach ability of the robot to the fixture also called the swept area of the robot (indicated by circular around robot). It also shows the constraints of space or the space available for the fixture that we are designing.
Layout provided information about flow of parts, station pitch, robot station, accessories like tool changers and tip dresser, sub assembly links, platform height, loading and unloading sequences.
Q) What is Ergo Data?
Ans: Ergo data is basically involved well manual operators are involved and every company has different type of standard for aggregate data so we will be getting that particular input from the customer so these are the standard that we follow so this kind of Ergo data we get from the customer.
Ergonomics: Ergonomics also know as human engineering and human factors engineering is the scientific study of the relationship between man and his working environments.
Objective of Ergonomics:
The fundamental objective of the study of ergonomics it to optimize the intergration of man and machine so as to improve the productivity and accuracy.
In short, the objective of ergonomics is designing for human use and optimize working and living condition
Two main objectives of ergonomics are:
- To enhances the efficiency and effectiveness with which the work is carried out so as to increase the convenience of use reduced error and increased in productivity.
- To enhances certain desirable human values including safety, reduced stress fatigue and improved quality of life.
Ergonomics Involves the design:
- Work place suitable for the worker
- Machinery and control so as to minimize physical strain on the worker to enable the improvement in the efficiency
- An environment for performing a task most effectively and conductive
- A conducive task and work organization.
Benefits of Ergonomics:
- Improve working condition
- Reduces physical workload
- Improve work postures
- Reduces efforts of certain movements
- Better reading instrument displays, handling of machine levers and control
Q) what do you understand by weld study?
Ans : Weld study means of the welding technique that we are going to use ,its temperature type of current type of gases used type of gun used for welding and where are we going to weld etc. If we use a spot welding what kind of electrode is used for welding number of spot etc come under the weld study of that particular component .
Weld study include :
- Weld gun details
- Weld matrix and weld points
- Geo weld point and respot weld points
Weld gun details:
- This involves the study of the gun like
- Type of weld it does
- Number of spots it can weld
- Temperature of the weld
- Type of current used
- Approach of the gun
Weld matrix and weld point: Weld points are basically where the welding is going to happen at which point at which coordinates is going to happens.
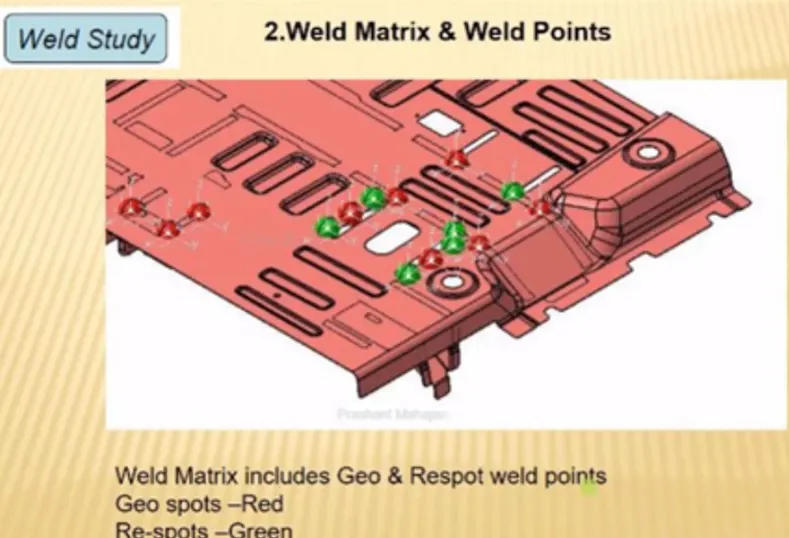
Geo weld points and Respot weld Points : The data of the weld Metrix and the weld point will be given to you in the former spheres ,red and green spears. At that points welding is going to happen. Geo Spots are Red in colour and Respot are green in colour. All the red spheres are going to happen in geostationary.
Q) What are the criteria for percentage completion in the designing stage? Explain it in details.
Ans :
- Percentage completion criteria are followed in the designing stage and dispatch stage of welding fixture. The percentage completion criteria contain the current status of a task, expressed as the percentage of the task’s duration that has been completed. you can entre percent complete or you can have project calculate it for you based on actual duration
- It’s followed in designing stages and dispatch stages of the welding fixture
- It ensures that how much task that we have decided to complete within the stipulated time is complete or not and how much of it is rest to complete and whether it is going to be complete or not in given time.
0-25% -Input and concept design:
This is initial stage of project. input data provide by customer like functional requirement, customer standard etc .and after studying those input the concepts of fixture design is created. After completion of this task about 25% of work completed.
25% -40% -Concept approval and simulation check:
As concept of fixture design is created and simulation checked it is sending for customer approval. Customer will study all simulations and gives his approval. if there are any changes required then it has to do accordingly and again submit for approval. This concepts design approval from the customer after study of simulation contributes only 15% of total design work. But with completion of this task 25-40% works completed.
40-85%-Design freezing and detailing:
This phase involve design freezing after approval of concept design. Freezing means finalizing concepts design. Then next step is detailing as per customer standard template with completion of this stage almost 85% of work is completed is designing stage.
85-100% -check and final dispatch:
After detailing the quality checking team starts inspection of all the data and it will dispatch to the customer it is ok as per customer standard. If there is in error in drafting it will create issue or mistake in manufacturing part.
Q) Brief about output in design?
Ans : it includes data to given to customer after completion of design stage. The output is 3D models and 2D drawing of the tool.
In the fixture elements design output contains detailed design of locators, detailed design of clamps, detailed design of support positions of locators, positions of clamps, positional of support if any type of locators, types of clamps, types of supports, clearing forces and support.
There are two types of tools in fixture design:
- Unitized tool
- Non unitized tool
Unitised tool: In unitized tool there are multiple units on common base for example geo fixture, checking fixture, hemming station etc.. Unitized tools require two types of sheet.
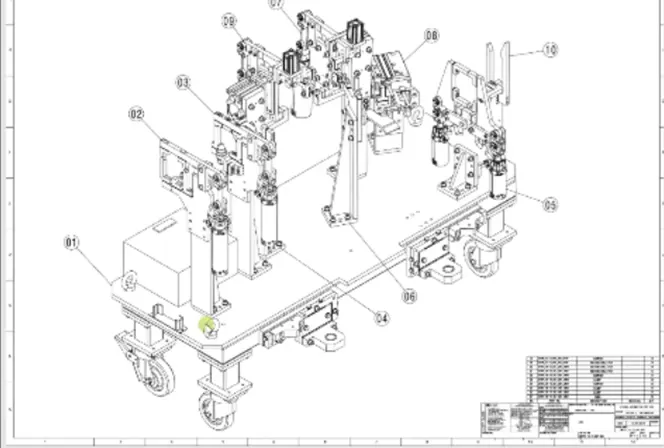
Key sheet: An index of units and their placement on the tool base. Key sheet shows placement and location of that particular unit on tool base where exactly and exact position of tool base. Key sheet is showing orthogonal or isometric view of that entire component.
Layout sheet: A detailed drawing of individual units to include all of their units . Layout sheet detailed drawing of that particular tool where we are going details of component. This also helps in CMM inspection of fixture .
Non Unitised Tool:
Non-unitized tools that can stand alone and can be detailed dodely on a layout sheet Cg Rack, take out trolleys, tum tables, grippers etc.
The output should compile following part :
- Approve standard parts should be used wherever possible. This saves lots of times, efforts and economical
- Design should be as simple and economical as possible. Geometry is complex then fixture design is complex but approach is trying to design as simple as possible.
- Design must comply with all current safety and ergonomics standard
- Design must provide for controlled and damage free handling of product .it should not damage other part
- Adequate error proofing provision must be incorporated in each design by providing switches, rough locator ele. Proximity switches are basically sensors which tell part is present or not in fixture rough locators work as Poka yoke to guide entire panel orientation.
- The weight of moving part must be kept to minimise while maintaining maximum strength. weight of moving component kept as minimum as possible but it should not compromise on strength. There is balance between these two things.
- Frames and structure are to be simple and sturdy
- Design clearances and accessibility for routine maintenance and service. Fixture need to maintain after certain period of time so it’s easily accessible for maintenances.
- Motion control must be consider on any moving equipment’s
- Designer is responsible to validate clamps and all weld gun.
Q) What do you understand by structuring a design tree? How Does it reduce error during the design process?
Ans: structuring a design tree implies to a process where all the assemblies and parts are named in a specific standard. Different customer have different set of standard to structure a design tree.
It is a important process which help us to identify a specific part or assembly as to which project, tool or unit, it belong to.
This help us to avoid the errors during study, manufacturing, assembly, inspection etc .
If the parts or assemblies are not named properly or the design tree is not structured properly, it will create confusion to understand the design and may create major possibilities of making an error .
Naming of a fixture or a unit or a part ,gives the information as to which project or zone or assembly do they belongs
It can help us to identify the quantity of items of same type or different types that are being used in an assembly for e.g. bolt .it actually tells you how many bolts are particularly required in that assembly or unit.Below figure shows design tree structure properly and component shows in key sheet ,Each unit has a separate name .
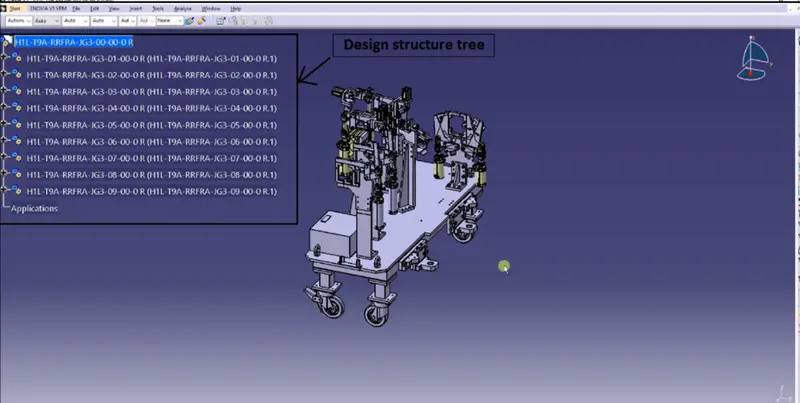
Every part, every component should be named according to their procedure
If we did a mistake or renamed the entire standard part from the customer as a design part. Now the customer going to manufacture the entire part again from the scratch but he already have that product in his itinerary but extra cost extra time and is feasible. This is also known as an error which actually going to increase the cost of the entire assembly as well
Naming a fixture or a unit or a part gives the information as to which project zone or assembly do they belongs
If we name the part properly or name the fixture properly actually tell which unit or which assembly or which zone or in which station it actually belongs.
In design tree in which designed parts are at top and all standard parts are at bottom.
`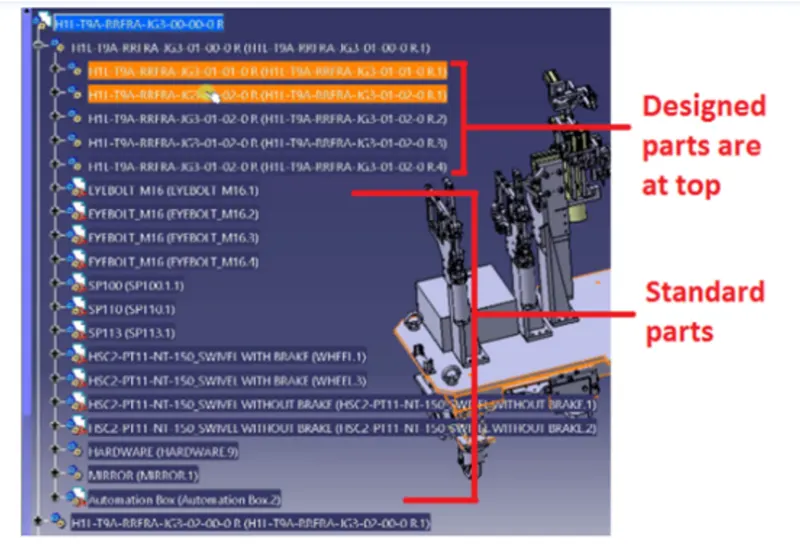
The blue highlighted number is H1L-T9A-RRFRA-JG3-00-00-00
- H1L-T9A- The project name
- RRFRA- Panel name
- JG3- Jig no.3
- 00-unit no
- 00-part no.
- 00-component no.
Under the product there are main assemblies sub assembled child parts etc these all parts are provided with specific number, zone etc to identify easily.
Q) What are units? Mention 5 type of units.
Ans: A unit is a device that has a specified function, especially one forming art of a complex mechanism, multiple units are joined together in order to form a fixture and are attached to a common base which serves as a common support to the units where they are fixed .
A welding fixture is assembly of different types of units.
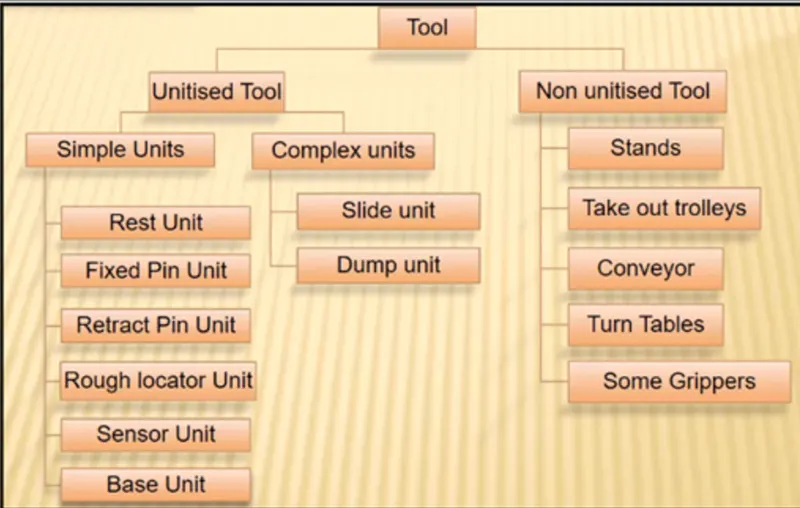
- Unitised tools
- Non unitised tools
Unitised Tools:
Unitized tools are basically tools which is part of multiple units or multiple tools inside it . These are the tools which has to be represented by two format i.e key sheet and layout sheet, Unitized tools are basically two types:
a.Simple Unit: Simple units will have a very simple design to it , then the approach of the designing and manufacturing is also very simplistic .Simple units are classified as :
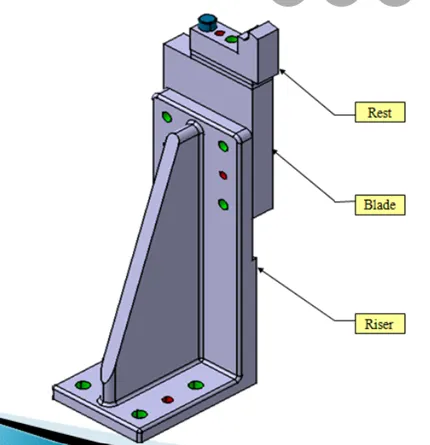
- Rest unit : Rest unit is basically a unit where the component is tested ,there is no upper clamp to it , there is no force applied to it .There is no cylinder attached to it usually it will have a riser a blade and few rest mylers.
- Fixed pin unit: Fixed pin unit is basically a unit which has a pin which is already fixed it cannot be moved .
- Retract pin unit: Retract pin unit is oppose to fixture which can be moved up and down by using a extricable pneumatic cylinder, so it can be retraced to certain distance.
- Rough Locators: A rough locator is a part designed to guide the operator to locate the car panel on the pins accordingly. A rough locator can be of standard part or make part.
- Sensor unit: A sensor units are used in actually sensing whether the panel or a particular component is there or not. For example if we are assembling component of 10 parts, each part will have a sensor or multiple attached to it .
- Base unit: A base unit is unit designed to mount all other units .
- complex units:
Complex units like slide unit is an example of a complex unit that design itself a little complex in design
Slide unit: The slide units are basically where the sliding mechanism is involved.
Dump Unit: Dump unit is basically like a conveyor where we assemble a component if we have a particular constraint.
non-Unitized tool:
Non unitized tools are basically one unit itself, which is basically don’t have any processes functionality to it is just to keep component on it as a stable, like gripper turntable stands etc non unitized tool
- Stand
- Take out trolleys
- Conveyor
- Turn table
- Some gripper
Q) Describe the fixed pin unit and their purpose?
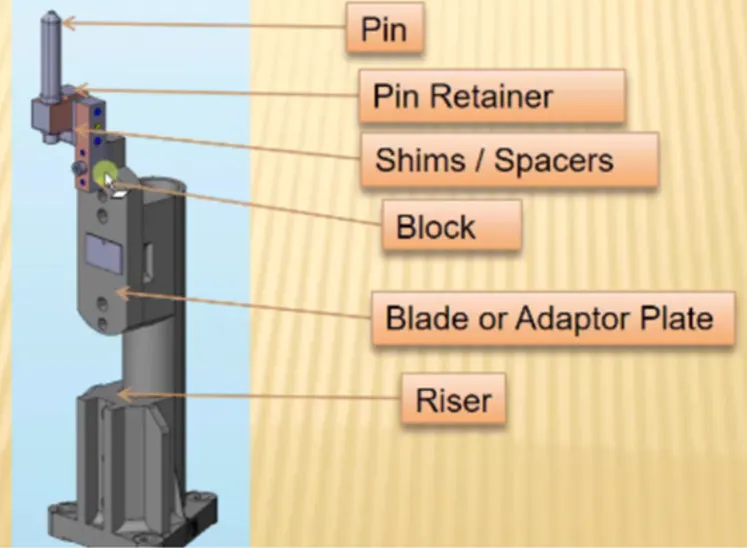
Ans : it is unit designed to locate car panel using pins.it is unit pin is already fixed it cannot move and below are different parts of the unit in general. Fixed pin unit basically have pin , pin retainer ,shims /spacers ,block, blade or adaptor plate. Pin retainer support that pin .
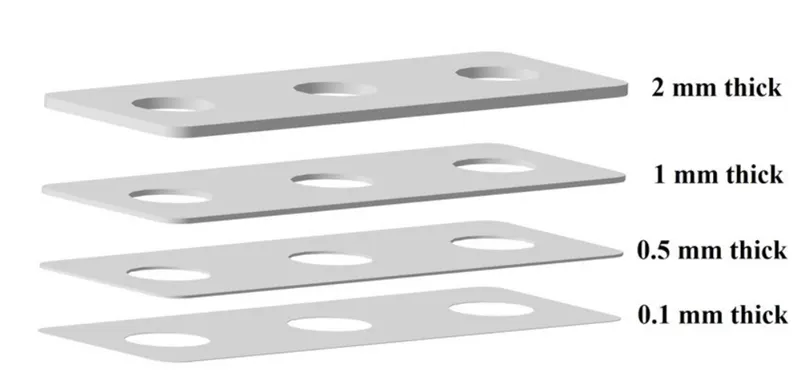
Every pin unit will have two directional shims. The block is used to mount entire pin unit. Shims are used to avoid stack up tolerance while assembling entire
Components shims are come in pack of 0.1,0.2,and 0.5mm
Purpose of fixed pin unit : Pin is most important part of fixture and used to restrict rotational as well as translational degrees of freedom that particular component. Purpose of fixed pin unit is to fix the panel translation motion along two axis and to prevent rotation of panel in the axis of panel.
It supposes to have exact coordinate for it to get fix. Suppose it will move by 0.1 to 0.2mm from its original positional then entire assembly will not happen or get rejected.
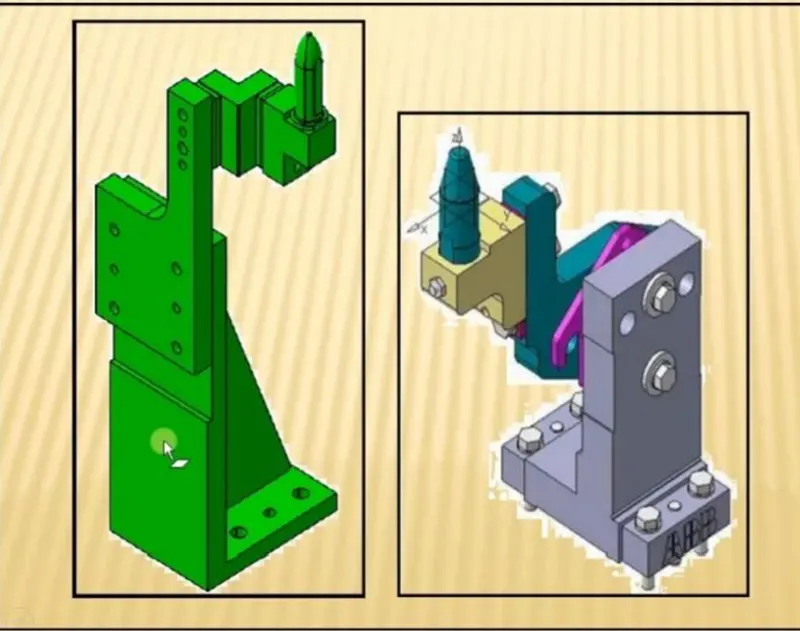
Q) What are the different parts of a fixed unit?
Ans: The different parts of a fixed unit are
- Locating pin
- Pin retainer
- Shims
- Blade
- Rise
Locating Pins:
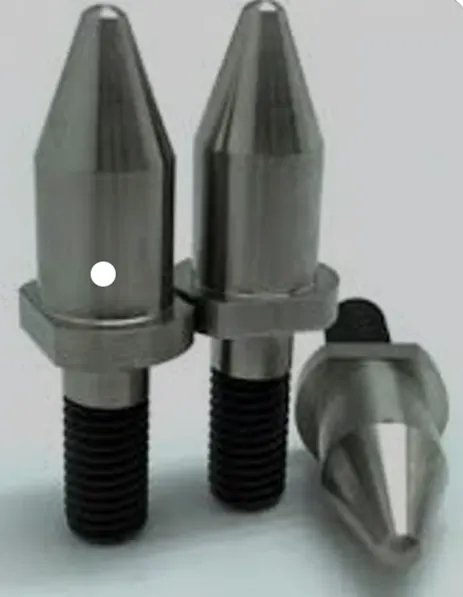
Locating pin are used for controlled, fine tolerance positioning of a work piece. Usually two locating pins are enough to properly locate the work piece on one plane. There are dozens of styles of locating pins that can be utilized in a design. Locating pins are a great way to make sure the parts you are putting together fit the way you want them to fit. Drill two holes opposite each other in each part ,install a cylindrical locating pin ,parts are aligned exactly the way we want if we are having alignment issues with using just bolts or other fasteners a locating pin can be a great way to firm up our assembly .
Risers:
Riser is a structure generally used to mount the toggle clamp and rest, clamp mylars and location pin. It is not necessary to have one riser where all the parts of clamp or rest or location units are mounted. Generally riser are either made of plate fabrication or plate and tube welding together or from single gas cut plate. These are generally manufactured to give height to the assembly.
Blade:
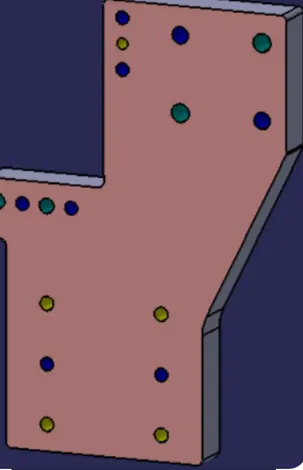
Blades are the plate attached to the riser. Parts like cylinder, arms etc are mounted on the blade. Chamfer is given to straighten the blade.
Shims :
Metal shims are used to finely adjust the location of how the fixture holds the product so that it is welded together within the dimensions set for the product to work well .
A pack of thin metal shim is placed between two components in the fixture. The first component is fixed in place and the second component is attached to the first component with the pack of shims in between. Removing one shims or adding one shim slightly adjusts the location of the second component. This is important to manufactures who want to have their products parts assembly easily after being welded.
Pin Retainers:
A pin retainer is a part which holds the pin in position the pin retainer can be either a make part or a standard part also. Pin retainer is used to hold the locating pins firmly.
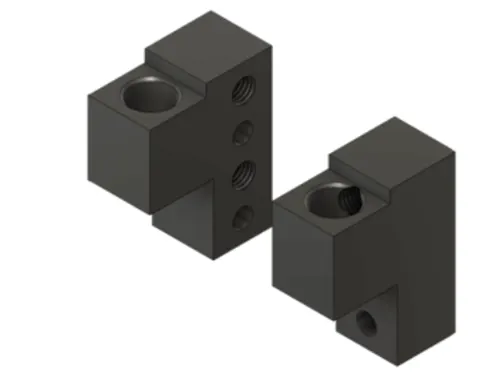
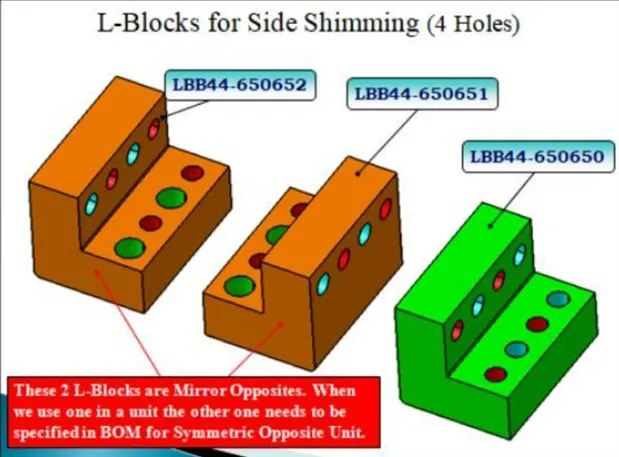
L-Blocks : L Block is used just to provide the necessary shimming for adjustment. In case of mounting an block we should check bolting access as there is already a bolt to tight the pin. Hence clear hole should be given from L Block .
Q) what is the purpose of making a rest unit and describe its parts?
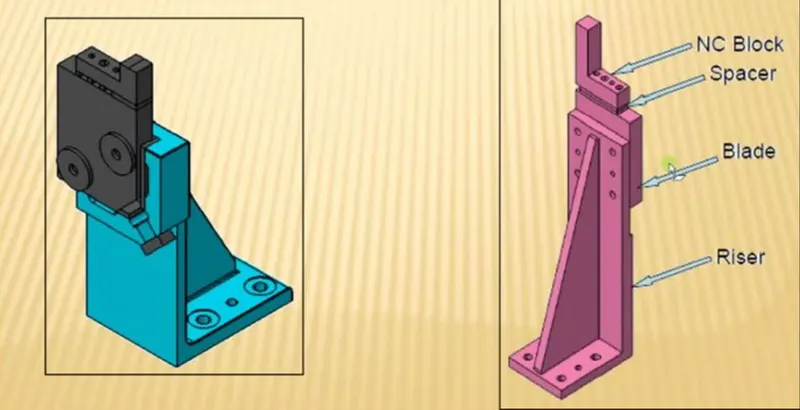
Ans: Rest unit is unit designed to support car panel using Mylar /NC block/rest component is rested only no upper clamp or force applied there.it is the simplest unit to design because it has fewer parts to design and the purpose is only resting of the car panel, because of this simplicity the rest unit is combined with other units to reduce the cost of the overall project.
It can be combined with clamp unit to clamp as well as to rest the car panel .it can be combined with locating the unit to locate as well as to rest the car panel. Also locating, clamping and rest unit can be combined together in one unit to reduce cost.
There are no cylinder attached to it. It has a rest Mylar, blade and riser and below is different parts of rest unit. The rest unit also divided into a simple support unit, multiple support units and a retractable support unit.
Mylar/NC blocks/Fingers:
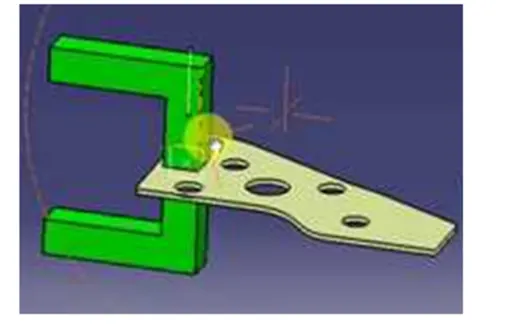
These are parts are used to hold panel. They are globally called as Mylar. Top side mylar is called as clamping mylar and bottom side called resting Mylar. Every clamping mylar should have resting Mylar. It is jaw type, it’s prevent panel from deforming while welding. it’s hardened to increase it’s worn strength.
Riser :
Riser can be of L -type, welded or square tube or frame type. These are basically manufactured parts are used to give height assembly. it’s machined at mounted ends only to save cost.
Blade:
These are plates mounted on the riser.other parts like cylinder ,arms etc are mounted on the blade.
Shims/Spacer:
Metal shims are used to finely adjust the location of how the fixture holds the product so that it is welded together within the dimensions set for the product to work well.
A pack of thin metal shim is placed between two components in the fixture. The first component is fixed in place and the second component is attached to the first component with the pack of shims in between. Removing one shims or adding one shim slightly adjusts the location of the second component. This is important to manufactures who want to have their products parts assembly easily after being welded.
Q) What are the basic fundamentals to design a sensor unit?
Ans: A sensor unit is a unit designed to sense the car panel by using electrical sensors. This signals from the sensors will be fed to the PLC and so the next process will be executed by this signal .
Fundamental of sensors unit design:
- Every single loose panel which are being welded in a tool should be sensed.
- Each panel should be sensed by 1 to 2 sensors depend on the size of panel, Preferred to be in diagonal opposite ends of panel .
- Every sensor should be mounted in a 3 direction adjustable way in general .
Some major sensor manufactures are IFM ,Pepperl-fuchs,SICK,OMRON etc .
Types of sensors used in general :
- Proximity sensors
- Laser sensors
- Photo electric sensors
Proximity sensors:
A proximity sensor is a non-contact sensor that detects the presence of an object (often referred to as the target) when the target enters the sensor’s field. Depending on the type of proximity sensor, sound, light, infrared radiation (IR), or electromagnetic fields may be utilized by the sensor to detect a target. Proximity sensors are used in phones, recycling plants, self-driving cars, anti-aircraft systems, and assembly lines. There are many types of proximity sensors, and they each sense targets in distinct ways. The two most commonly used proximity sensors are the inductive proximity sensor and the capacitive proximity sensor.
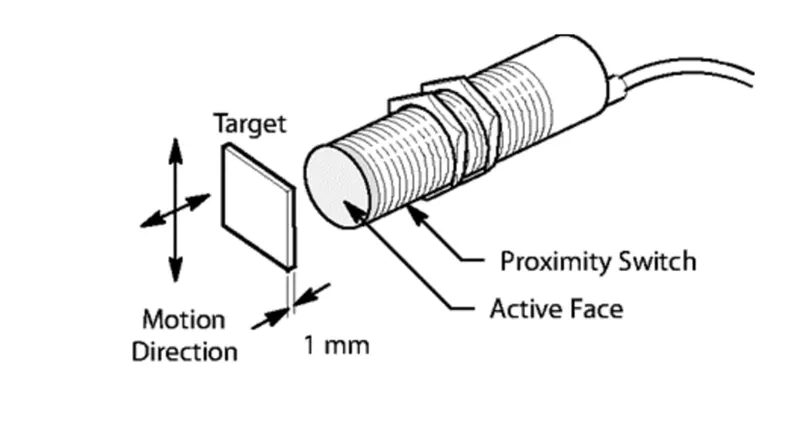
It has a sensing range 5 to 6 mm. It is based on the magnetic field principle.
Laser Sensor:
Laser sensor is a kind of sensor which uses laser technology to measure. It is generally composed of laser, optical parts and photoelectric devices. It can convert the measured physical parameters (such as length, flow, speed, etc.) into optical signals, and then use photoelectric converter to convert the optical signals into electrical signals. Through the filtering, amplification and rectification of corresponding circuits, the output signals can be obtained, so as to calculate the measured quantity.It has a sensing range id farther away from the proximity sensor.
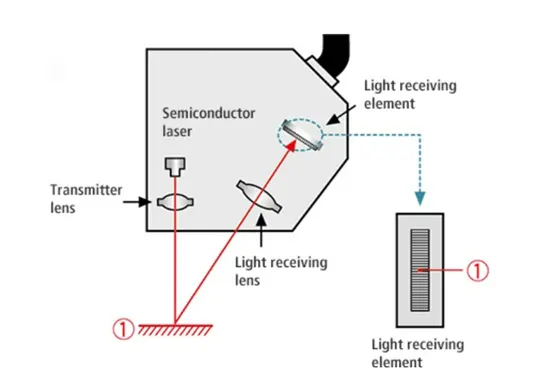
Photo electric sensors:
Photo electric sensor detect objects, changes in surface conditions, and other items through a variety of optical properties. A Photoelectric Sensor consists primarily of an Emitter for emitting light and a Receiver for receiving light. When emitted light is interrupted or reflected by the sensing object, it changes the amount of light that arrives at the Receiver. The Receiver detects this change and converts it to an electrical output. The light source for the majority of Photo electric sensor is infrared or visible light (generally red, or green/blue for identifying colours).
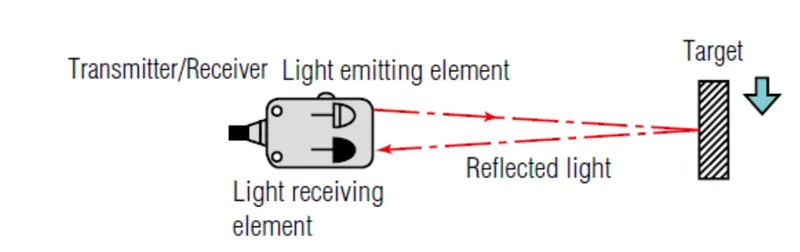
Q) What is rough locator unit and what are the basic fundamentals to consider while designing it?
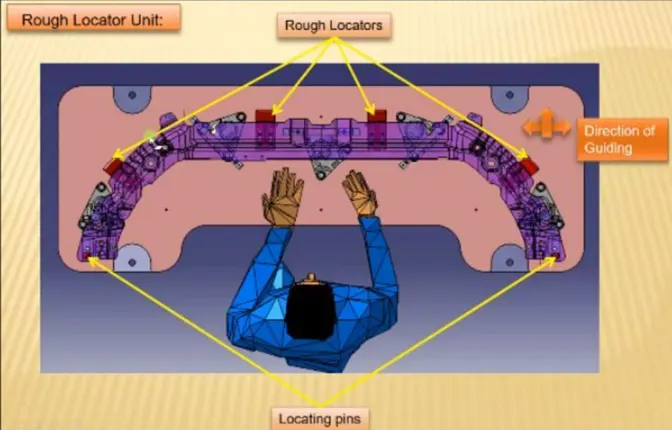
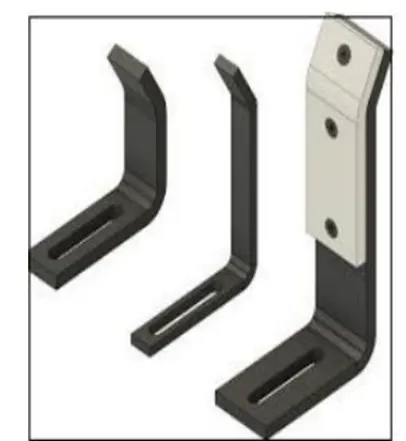
Ans : A Rough locator is a part designed to guide the operator to locate the car panel on to the pins accordingly. A rough locator can be of standard part or make part .
Fundamentals of Rough locator design:
- Rough locator should be placed at the edge of the car panel ,which it has to guide .
- Rough locators has to be placed in the same angle of the car part edge with a minimum distance of 2-5mm from the edge of the car part .
- Rough locator should guide the panel in pin arresting direction (in general)
- Rough locator should start guiding the panel before 10 to 15mm to the start of the pin engagement.
- Rough locators should be designed with entry angle for car part entry
- Rough locator should be designed with two slots to mount for easy adjustments. (In general)
- The slot should be in the direction of car part guiding.
Q) What is base unit and describe it’s parts ?
Ans: A base unit is the unit designed to mount all the other units (clamps unit ,In unit ,Rest Unit) ofd the tool,also other parts necessary for tool pneumatic valve box ,turnking cable path will also be mounted onto a base unit.
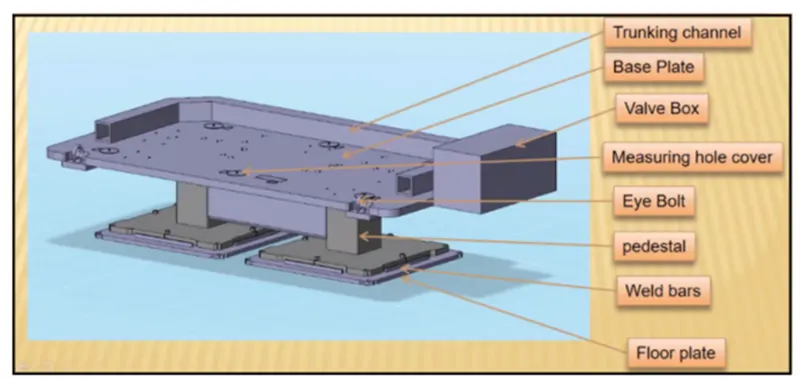
Parts of base units:
Parts of base unit are as follows:
- Valve box
- Trunking channel
- Measuring hole cover
- Eye bolt
- Pedestal
- Floor plates
Valve Box :
Valve box basically a box which supplies air to all the pneumatic cylinders assembled in the fixture .valve box consist of one solenoid valve is used to collect the air from the Pneumatic cylinder to valve box.
Trunking Channel:
Trunking channel is a kind of cable duct which help to guide and protect the wirings /tubes used in the fixtures.
Measuring hole cover :
In the measuring hole cover the coordinates points are engraved on it. The hole which mention the coordinates given the position placement of the particular unit . The measuring hole helps in CMM inspection and QC inspection.
Eye bolt:
An eye bolt is a bolt with a loop at one end. They are used to firmly attach a securing eye to a structure ,so that ropes of cables may then be tide to it for lifting purpose .
Eyebolt is used to frag or lift the base unit while relocating.
Pedestal:
Pedestal is a stand like structure where the entire unit of the base will be mounted.
Floor plate :
Floor plates is used to mount the entire base with floor. also helps to achieve the flatness of the fixture. Hence the base unit and their parts are explained in detail.
Q) What is Dump unit and what are its function?
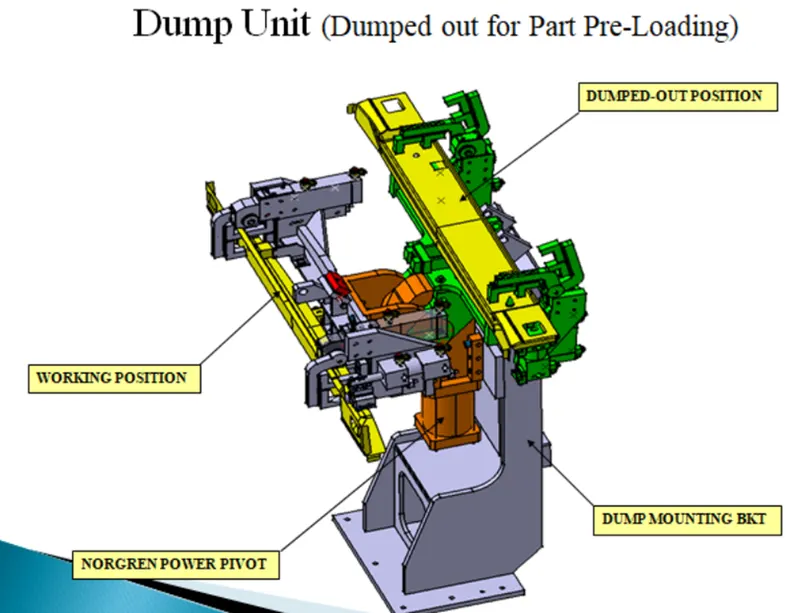
Ans: Dump unit is found in complex fixture
- A dump unit is used when there are Geometrical constraints while placing a panel
- A dump unit is used when there are geometrical constraints while placing a panel
- It consists of a dump cylinder to perform clamping and unclamping operation
Q) What is a slide unit? Mention where slide units are commonly used?
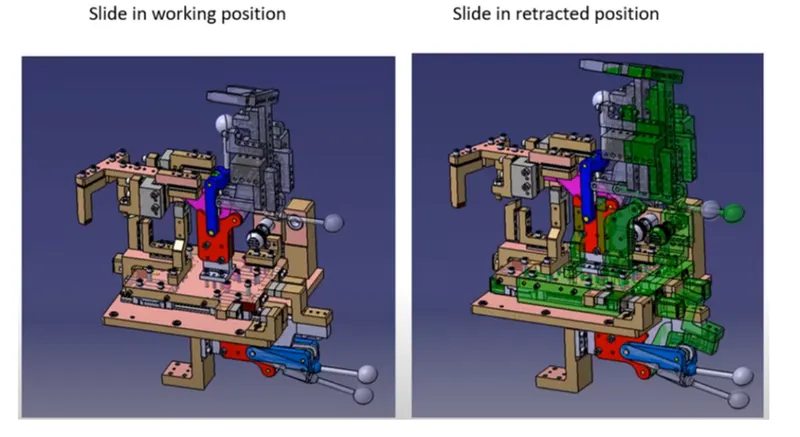
Ans : Sliding unit consists of cylinder cylinder. It slides between open and close position. At the end it has shock absorber and after that hard stopper. It has guide rail. It uses sliding mechanism. It also has position locking unit for maintenances purpose doesn’t allow to move entire unit and sensor unit to sense entire component reached at either side or not and stopper block to control moving.
- Sliding units are used in a fixture when there are a lot of space constraint, where usage of different units is very difficult in order to design the assembly.
- The sliding unit consists of a sliding cylinder to which a panel is attached
- The panel moves on the guide rails provided and this motion is due to the reciprocating motion of the cylinder
- The position locking units are used to lock the position of the panels on the guide rails
- Sensor units are used to detect the position of the sliding plate whether it has reached the desired position or not
- A stopper block is used to control the motion of the sliding plate