Week 3:- BiW Fixture Design Methodologies Challenges
1
Design Methodology in Technology
While design methodology is employed in many industries, it is commonly applied in technology fields, including those using the internet, software and information systems development. Several design methodology approaches have developed in the technology industry. Each was a reaction to a different type of problem. Some common technology design methodologies include:
- Top Down Design or Stepwise Refinement: This starts from the end solution and works backwards, refining each step along the way.
- Bottom Up Design: This methodology starts with a foundation and works up towards a solution.
- Structured Design: This is an industry standard. The technique starts by identifying inputs and desired outputs to create a graphical representation.
- Structured Analysis and Design Technique: This approach utilizes a diagram to describe the hierarchy of a system's functions.
- Data Structured Systems Development: Data structure determines the system structure in this methodology.
- Object Oriented Design: This methodology is based on a system of interacting objects.
Possible Careers using System Design Methodologies
- Graphic Designer: Graphic designers create and implement visual concepts through computer software. They generate artistic ideas that captivate and appeal to a target audience - often to sell a product or service.
- Art Director: Art directors are responsible for the visual layout and style of print publications, products, and media productions. They often come up with the overall design idea, directing others who produce the actual artwork and visual elements.
- Multimedia Artists and Animators: Multimedia designers and animators create moving images for visual media. These can include video games, film, and television.
- Web Developers: Web developers create and design websites. They are not only responsible for how it looks - but how it performs, implementing system design methodologies that optimize its speed and traffic capacity.
Common Skills Required for System and Program Design Methodology Fields
To work in the field of design, one not only need artistic abilities (this is crucial for generating creative visual concepts that appeal to a target audience), they must also display excellent communication, analytical, and time management skills. Having good interpersonal skills are beneficial for understanding the client and their needs, along with working and collaborating with other designers. Being analytical with their work can help one cater to the interests of the consumer, and the ability to manage time efficiently can help in juggling multiple projects with varying deadlines. Some careers in this field can also require knowledge of programming methods and languages.
2
First understand scope of the work. Means what is expected by customer. Every customer has its specific requirements and it may have own raw material, electric, pneumatic,cad, design standards.Every customer also gives different inputs and expects output e.g 2d drawing, process sheet in xls, pdf, CAD format of design, layout format, OLP.
- Bill of material (BOM) of the components to be welded- spot welding
- CAD panel data or at least 2D drawing of assembly and individual panel data
- Sheet metal panel thickness.Plays major role to decide 2 metal or 3 metal weld.
- Spot Detail information like total no of spots and spacing between the spots.
- Weld information clarity from drawing like 2 metal or 3 metal welding
- PLP (Principle location scheme) of the individual panel and total assembly.
- Cycle time - if calculated or can be found out as per manual or robotic welding process.
- Process sheet if Process engineering is done - where loading sequence, no of clamp data and gun data is mentioned.
- All clamping cylinder and fixtures standards.
- CAD -Software guidelines
- Raw material standards
- Design guidelines
- Bought out item(Purchased parts) standards like pneumatic items, toggle clamp, bearing, screw, dowel etc company information
3.
Geometric dimensioning and tolerance (GD&T) - GD&T will be given of the part for which we need to design the fixture . it will provide information about locating pin , sequence of opening of clamps , rest , dump and slide stroke information
Parts list - Part list will give us detailed information about the parts involved in the fixture . it will give us information like part name , part number , thickness of part , quantity of parts etc .
Cad files - Cad files of the part gives us information of 3d model , design analysis result . this information is very uselful as it will give us an idea on starting to design a fixture .
Clamp plan - Clamp plan is very important information as it will give us idea of places where we have our clamps , pins , dumps , rest etc . we should never change the clamp position unless we ask the customer and they agree to it .
Product assembly process sheets - In product asssembly process sheet , we will find what kind of products we are going to assemble for the particular unit or the component . The sequence of the assembly will also be given in this sheet .
4.
-A clamp is a device which is used to hold the workpiece . it is a force actuating mechanism of the fixture .
- A clamp plan is a very important input from the customer , the clamp plan will give us information about area where the clamps will be fixed to ensure proper geometry of workpiece is maintained during the operation .
- clamp plan provides information on location of pins , rest , clamps ,dumps etc . the coordines will also be mentioned in the clamp plan , so the design team can take the coordinates directly and start working on the fixture .
- We cannot change the clamp plan that is given by the customer , we have to inform the customer and if they agree then we can change it .
5.
- Layout is the most effective arrangement of the machines , processing equipment , service department to achieve maximum efficiency of the 4 M ( men , material , machine and method ) in the plant .
- It will give the floor plan of how and where the machines will be placed , position of robots , storage racks , etc . it will also show the reachability of the robots to the fixture which is called as swept area of robot .
- Layout also provides information of flow of parts , station pitch , robot stations , tool changers , tip dressers , loading and unloading sequence .
6.
- Ergonomics is the application of psychological and physiological principles to the engineering and design of products , processes and systems . the goal of human factor is to reduce human errors , increase productivity and enchance safety and comfort with specific focus on interaction between human and rhing of interest .
- In any operation , the workers or operators attain various postures , exerts force and work continously in a cycle time to perform a particular task . this may cause high level of strain to the operators . to avoid this the principle of ergonomics is applied in every operations wherever a interaction of human with machine is involved .
- so the ergo data is the input which gives human factors engineering data between operator and its working environment .
- It has various benefits like improved working condition , reduce physical workload , improved work postures , reduced efforts of certain movements etc .
7.
- Welding is a process which is widely used in automobile industry for joining of parts together , so a welding fixture is necessary to be made so that the geometry of the part does not change during the welding process .
- weld study includes study of weld gun and the weld matrix and weld points , geo spot and respot weld points .
- weld gun study will give information about type of weld , temperature , type of current , approach of gun etc . weld matrix and the weld points will give us information on exactly where the welding will be done .
- There will be two welding stations , geo spots and repots . geo spots will be the first round of welding operation , after this respot is done on the places where we could not weld in the geospot station .
8.
- 0 - 25% input and concept design - We will get the inputs from the customer and by studying these inputs we will create a concept design of the fixture .
- 25 - 40% concept approval and simulation - We will get the customers approval on the concept and we will also perform various simulations on the design .
- 40 - 85% design freezing and detailing - once the customer has agreed and approved on the design we wil freeze the design and we will start with the 2d detailing of the parts . once we have made all the parts , we will assemble the whole model .
- 85 - 100% check and final dispatch - we will start the quality check on our fixture , then we will check the working of the fixture to see if it gives the intended output , once all the checking work is done we will diassemble the assembly and pack it properly and dispatch it to customers facility .
9.
After the designing phase of a particular product , we not only make a 3d model but we also have the simulation results performed on the model , we also make 2d detailed drawing sheets of all the parts that we have created , BOM, assembly sheets , etc . there are two types of tools -
- Unitized tools - Unitised tools require two types of sheets that is key sheet and layout sheet . key sheet shows the index , placement and location of particular units on tool base . layout sheets is the detailed drawing of individual units to include all their component .
- Non unitized tools - Non unitized tools are the tools like stands , tool changers for which you dont need the key sheet. it is the tools that can stand alone and can be detailed completely on the layout .
10.
Structuring a design tree is the process of naming all the assembly and parts in a systematic way and a specific standard . every customer has its own standard to structure a design tree .
- If the parts or the assemblies are not named properly or it is not structured properly , then this will create a lot of confusion to understand the design .
- So structuring a design tree is very important as it helps us to easily identify about the part or a assembly belongs to which project . it can also help us to identify quantity of items of same type or different type used in assembly .
- From the above image we can see that the designed parts are at the top and the standard parts are below .
- Blue highlighted number - H1L -T9A-RRFRA-JG3-00-00-00 , this is the product description or name
- here H1L-T9A is the project name , RRFRA is the panel name , JG3 is referring to the jig number that is jig 3 , 00 is the unit name . 00 is the part number , 00 is the componenet no .
11.
A unit is a device which has a specific purpose , and is also a part of a complex assembly . the BIW fixtures is a assembly of many units , this units perform different functions . units are of two types unitized and non unitized tool .
- The units have specific function like resting the panel , clamping the panel , locating the part , etc .
- Fixed pin unit - It is the non movable locating unit used for proper location of part and it arrests all the movement of part as well .
- Retract pin unit - It is a movable locating pin unit which has retracting mechanism , this helps in ease of assembly of two components placed in different direction .
- Rough locator unit - It acts as a rough guide so that the operator can mount the workpiece in proper place .
- Rest unit - Rest unit makes the panel rest on it .
- Base unit - It is the unit on which all oyher units are mounted .
12.
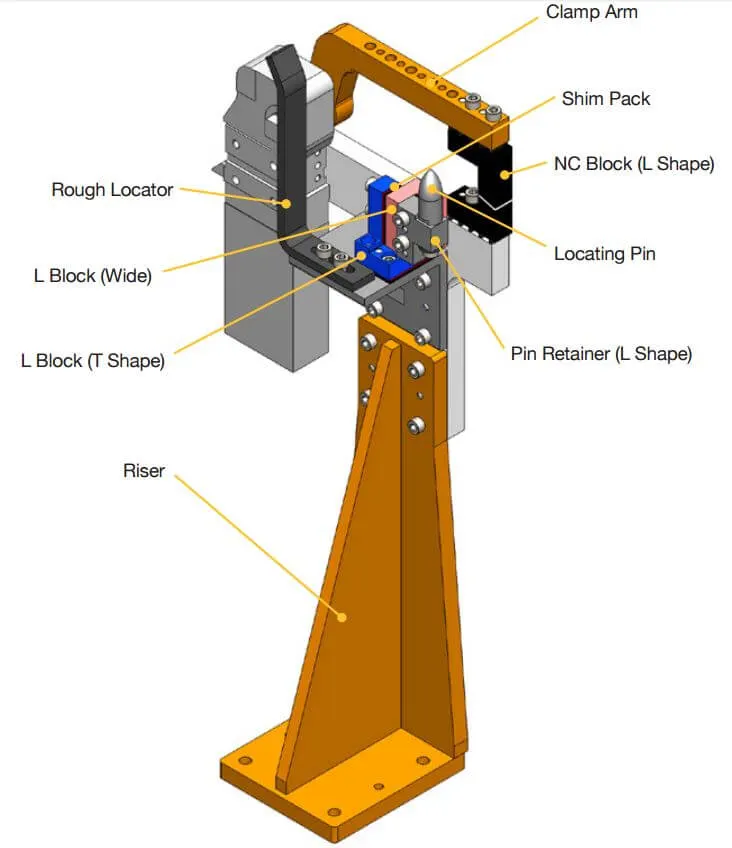
- Fixed pin unit is a non movable locating unit used for proper location of part and it arrests all the movement of part as well. fixed pin unit consist of pin , pin retainer , shims/spacer , block , blade or adaptor plate ,riser . Riser is the part which is used to rise or increase the height of the unit . blades is mounted on the riser . block will be mounted on the blade . shims are small spacers which are used for stack up tolerances . shims are made of various thickness like 0.1,0.2,0.5mm etc . pin retainer will hold the pin . and the pin is used to locate the part and restrict its motion .
- Purpose of fixed pin unit - The main purpose of the fixed pin unit is to locate the car panel and restrict its motion . it is placed following the 3-2-1 principle , so it is necessary to have two pins like 1 pin will restrict 4 d.o.f (4 translational) and the other pin must restrict 2 d.o.f ( 2 rotational) .
13.
Pin - Pin or locating pin is used for location or positioning of workpiece in correct manner . this pin is made of precise dimension and tolerance . usually two pins are enough to locate a workpiece on a single plane . There are many types of locating pins available . it is upto us what kind of pin will work for our workpiece
Pin retainer - A pin retainer is a part which is used to hold the pin firmly and in position . a pin retainer can be a make part or a standard part also .
- shims/spacer - Shims and spacers are plate of varying thickness which is used for compensation of stack up tolerance that is in assembly . the thickness of shims is 0.1mm , 0.2mm, 0.5mm , etc . sometimes in an assembly stack up tolerances is generated , this needs to be corrected so we use shims and spacers .
- Block - Block can be machined to any thickness , this depends on the design of fixture and for what reason we want the block .
- Blade - Blades are plates attached to the risers , parts like cylinder arm etc are mounted on the blade .
- Risers - Riser is a standard part which is used to rise up the height of whole unit .risers are generally made of plate fabrication or plate and tube welding or from single gas cutting .
14.
Rest unit is designed to support the car panel using using myler , NC block . It is the most simplest unit as it has only few parts like NC block, spacer/shims , blade,riser . because of simplicity in design it is combined with other units to reduce the number of parts which will reduce cost . it can be combined unit so that it can clamp as well as rest the part , it can be combined with locating unit to locate as well as rest the part . the differet parts of the rest unit are -
spacers/ shims - Shims and spacers are plate of varying thickness which is used for compensation of stack up tolerance that is in assembly . the thickness of shims is 0.1mm , 0.2mm, 0.5mm , etc . sometimes in an assembly stack up tolerances is generated , this needs to be corrected so we use shims and spacers .
Risers - Riser is a standard part which is used to rise up the height of whole unit .risers are generally made of plate fabrication or plate and tube welding or from single gas cutting .
NC block/ Mylars - It is a part which is used to hold the panel from top and bottom . mylars are of two kinds clamping mylars and resting mylars . mylars have a jaw type shape , which improves the holding of part . mylars are also known as fingers . it wont allow the deformation of the part during the welding processes .
15.
A sensor is a device which detects or measures a physical property , and records , indicates or responds to it . a unit which is designed to sense a object is called as sensor unit . the information from the sensor is send to the PLC . a sensor is sensitive and can be damaged so a sensor cover is provided to it . there are different types of sensor like proximity sensor, laser sensor, infrared sensor , photoelectric sensor etc .
-Fundamental to design a sensor unit -
- Every single loose panel which is being welded by the tool should be sensed .
- Each panels should be sensed by 1 or 2 sensors depending upon size of panel .
- Every sensor should be mounted in a 3 direction adjustable way in general .
16
Rough locator is a device which is used to guide the workpiece in proper place . this rough locators is mainly used when manual operator is present but it is also used in automation . rough locator act as a foolproofing method .
- Fundamentals considered while designing rough locator -
- Rough locator should be placed at edges of car panel , which it has to guide .
- They should be placed in a same angle of car edge angle , and minimum of 2-5mm distance should be maintained from edge of car panel .
- It should guide the panel in locating pins .
- Rough locator should start guiding the car panel before 10-15mm from start of engagement .
- Rough locator should be designed with entry angle for car panel , which is generally 30-45 degree .
- The rough locator should be designed with two slots , for easy adjustments .
- The slot should be in direction of car part guiding .
17.
Base unit parts are given below -
- Floor plate - Floor plate is used to mount entire base with floor . it also helps to achieve the flatness of the fixture .
- Weld bars and pedestal - Pedestal is a structure where entire unit of base will be mounted .
- Eye bolt - Eye bolt is the bolt with a loop at one end . they are used to firmly attach a securing eye to the structure. when the whole fixture table has to be moved from one place to another , cables are attached to this bolt and the fixture table is moved .
- Measuring hole cover - The base plate has several holes for mounting of units on it . this holes are measured by CMM machine to check if their position is accurate or not . a plate is used to cover the hole so that no dust or other particles can damage the hole .
- Valve box and trunking channel - Valve box supplies air to all the pneumatic cylinders in the assembly . a valve box consist of solenoid valve which is used to collect air from pneumatic cylinders to valve box .
- Base plate - A base plate is a heavy plate of large thickness because it carries weight of the entire assembly . it is machined to maintain parallelity and it also has holes drilled on it to mount the units
18.
Dump unit is a complex unit which is used in places where there is a space constraints or some other constraint . when we have some geometrical constraints and we cannot mount clamp unit, rest unit etc in a normal way then dump unit is used . It consist of dump cylinder to perform operation of clamping and unclamping of car panel .
Functions of dump unit -
- When there is a particular constraint and we cannot asssemble component in normal way dump unit is used .
- It has a dump cylinder which performs the opening and closing action . it has a clamp cylinder unit too .
- This dump unit is complex in design and so it is used only in need .
19.
-Slide units are positioning unit which are used to position the car part or panel , units , robots , for further operation . sliding units are used in places where we have space constraint and differnt units cannot be used so we use sliding unit . It consist of foll parts -
- Sliding cylinder - this is used to move the panel from open position to close position and vice versa .
- Position locking unit - It is used to lock the plate at a particular place and it will not allow it to move .
- Guide rail - It is used to guide the plate to move from one position to next ,
- Stopper block - It is used to control the motion of sliding unit .
- Sensor unit - It is used to sense whether the component is moving properly or not .