Week 3:- BiW Fixture Design Methodologies Challenges
1) What is design methodology?
Ans: Design Methodology: Design methodology is basically the stages or steps to be followed while design a product. We will get confirmation from customer and certain inputs from him and we will proceed further for designing and then after completion of project we will give some technical and non-technical documents to customer as design output.
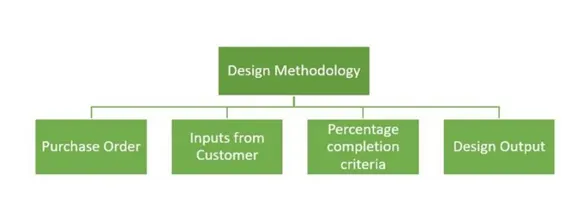
Fig shows design methodology chart
a.Purchase order: Purchase order is basically confirmation from customer side that we are ready to start work. A purchase order (PO) is a commercial document and first official offer issued by a buyer to a seller indicating types, quantities, and agreed prices for products or services. It is used to control the purchasing of products and services from external suppliers. Purchase orders can be an essential part of enterprise resource planning system orders. Indent is a purchase order often placed through an agent (indent agent) under specified conditions of sale. The issue of a purchase order does not itself from a contract. If no prior contract exists, then it is the acceptance of the order by the seller that forms a contract between the buyer and seller.
- Input from customer: Inputs from customer are major input that we get from customer. We study those input to what kind of information get out of it.
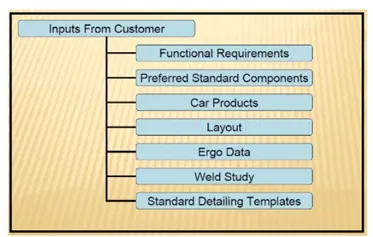
Designer needs following basic information to start the BIW fixture:
- First understand scope of the work, means what is expected by customer. Every customer has its specific requirements and it may have own raw material, electric, pneumatic, cad, design standards. Every customer also gives different inputs and expects output e.g., 2d drawing, process sheet in xls, pdf, cad format of design, layout format, OLP.
- Bill of material (BOM) of the components to be welded-spot welding.
- CAD panel data or at least 2D drawing of assembly and individual panel data.
- Sheet metal panel thickness plays major role to decide 2 metal or 3 metal welds.
- Spot detail information like total no of spots and spacing between the spots.
- Weld information clarity from drawing like 2 metal or 3 metal welding.
- PLP (Principal location scheme) of the individual panel and total assembly.
- Cycle time if calculated or can be found out as per manual or robotic welding process.
- Process sheet if process engineering is done-where loading sequence, no of clamp data and gun data is mentioned.
- All clamping cylinder and fixtures standards.
- CAD – Software guidelines.
- Raw material standards.
- Design guidelines.
- Bought out item (Purchased parts) standards like pneumatic items, toggle clamp, bearing, screw, dowel etc company information.
c. Percentage completion criteria:
- It consists planning of completion of total project. How much days the project will take to complete.
- It is followed in designing stages & dispatch stages of the welding fixture.
- It ensures that how much task that we have decided to complete within the stipulated time is complete or not & how much of it is rest to complete & whether it is going to be complete or not in given time.
d. Design Output:
- Output consists 3D models, 2D drawing which is the detailing part, BOM & other related documents.
- There are some tools which are multiple units on common base are called in unitized tools for ex fixture which includes no of units on the same base.
- They required two types of drawing sheet as follows.
- Key sheet – It shows the index of the unit & their placement on tool base.
- Layout sheet – It is the detailed drawing individual unit to include all their components.
- Non unitized tools which can be completely detailed on layout sheet.
2.What are the inputs required from the customer to start designing a Fixture?
The inputs that we get from the customer to start the designing of the fixture are as follows
- Functional Requirement
The inputs regarding the functional requirement of the fixture are received from the customer like for which process the fixture needs to be designed. For example, welding fixture, gluing fixture, Checking fixture Etc.
- Preferred Standards
The customer wants to follow some standards. These standard parts should be used in our design which saves time and money spent on the project.
ABB , NAAMS , Tunkers are some standards
Some components like Clamps, Cylinders, switches, etc are used based on the preferred standards of the company.
Car Products
The inputs regarding GD&T, part lists, Clamp plan, Pin Locating Points, Product assembly Process Sheet are received by car products.
GD & T
It gives information about the location of pins, Rest, clamps, and slide unit information of each station.
Parts lists
It gives information of part like part name, the part number of the part which is to be assembled in the fixture.
Clamp Plan
Clamp plans give the location of pins, rests, clamp, dumps, etc. we need to consult with the customer if we need to make changes in the clamp plan.
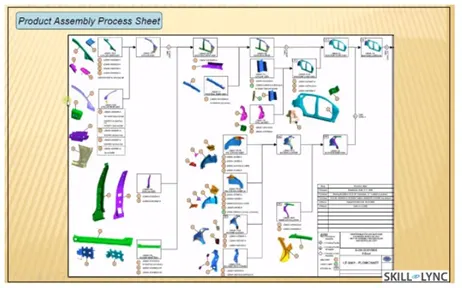
Product Assembly process sheet
It gives details about the sequence of the assembly of parts in the various stations.
CAD Files
The 3D model of the car part is required for designing the fixture for that particular part.
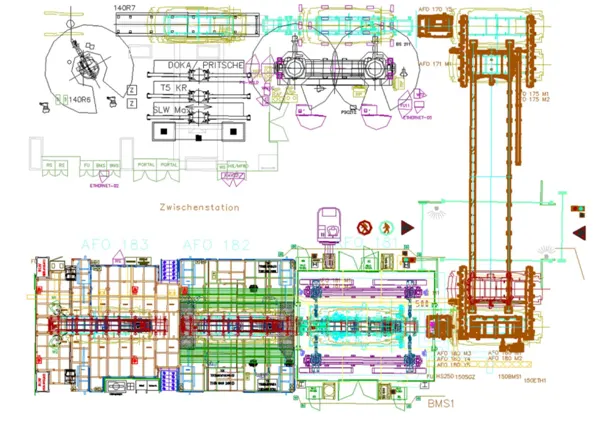
Layout
The layout provides information about the flow of the product, assembly sequence, the position of robots, sub-assembly links, accessories like tool changer and tip dresser, platform height.
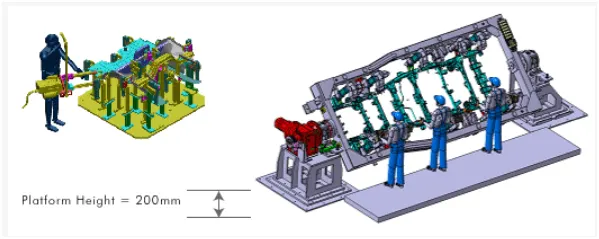
Ergo data
- Ergonomics defines as the study of human behavior and movements.
- The ergo data like the height, distance from the fixture is given as an input by the customer and the design of the fixture must adhere to these data.
- This design will result in ease of operation for the operator of the fixture.
- Weld Study
Weld study gives information about the type of weld gun to be used for the process. Also, it gives information about the number of geo weld spots as well as the number of Re-spot welds. These spots will be indicated using red and green spheres respectively.
3. What is the input we get from “Car products”?
Ans: The inputs that we get from the ca products are as follows:
- GD&T
- Part Lists
- CAD Files
- Clamp Plan
- Product Assembly Process Sheet.
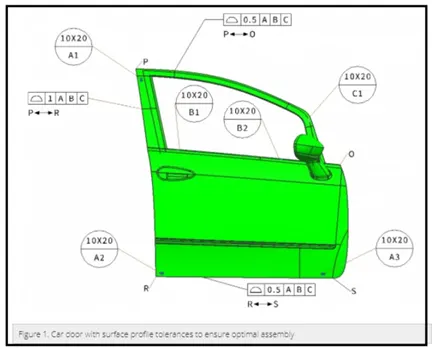
1. GD&T: Geometric dimensioning & tolerance of the part for which the fixture has to be designed. GD&T provides information about locating pins, Rest, Clamp, Dumps & slides information of each station & sequence & opening of clamps, Dumps & slide stroke information.
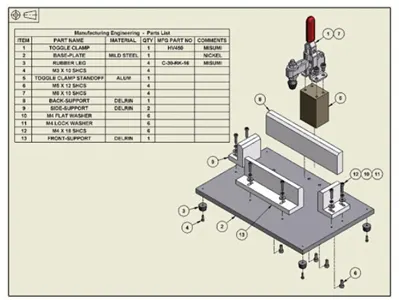
2. Part list: Part list is nothing but listing down all parts of assembly. It includes information about the part name, part number, Tooling revision, Part thickness etc. Suppose first assembly has gone between hood inner panels & latch which going to attach next hinge going to attach. So, there are different list of assembly we are going to perform. So, every assembly will have different fixture unit.
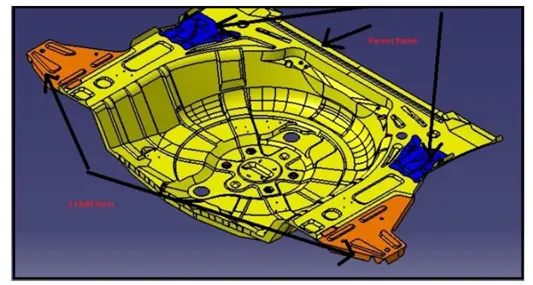
3. CAD File: 3D file of that car product requires from customer. The 3D model file of the car part is given from the customer to study on it. The car part is designed by using 3D modelling software. From this we can get some conceptual idea of the designing of fixture. The model is going to be the base of the fixture design.
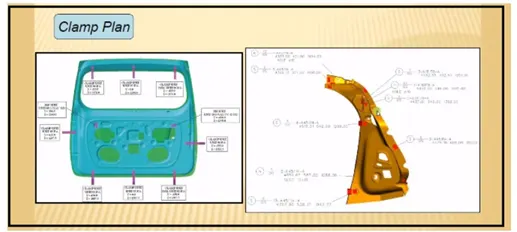
4. Clamp plan: It provides information about position of clamp unit, per unit, rest unit, dump unit, etc, this is major input from customer & it should be never be changed without permission of customer. Clamp plan provide exact location of pins, rest, clamp etc. It is in more detail, it gives exact location in X, Y, & Z co-ordinates value to start designing.
5. Product assembly process sheet: Product assembly process sheet is sheet that gives following details.
- Part assembly sequence
- Sequence of operation
- Cycle time
It gives detail process of the completion of the part from scratch to the finished product assembly. It will give detailed plan of component how they welded as well how product is moving from one assembly to other & this process plan should not be changed without permission of customer.
4.What is the Clamp plan?
Clamp Plan:
Clamp Plan is very important input that we get in the car products is where exactly we can place those clamping units are the particular pin Units.
- We should never change the position of the particular clamp or the pin, which is given in these data.
- We can change our design a little bit here or there, but we should not change the input design data about the clamp position or the pin position.
- In the Clamp plan there is clamp unit, pin unit and it is more detailed. It also gives the exact location of y and Z coordinates designing as well you can just input these coordinates and you can start designing from there.
- If the three coordinates, whole diameter and everything is already given to design the entire future design phase, and it sometimes ministry as well. It happens that another thought position, also given very close to the clamp, or the clamp location. So always ask to whether you have changed the clamp position.
- You should never change the vent position or the clamp position without asking it So always be vary about these situations So the tool might get damaged or department get damaged so for that itself need to clarify once again before doing any changes in the clamp.
5. WHAT IS A PURPOSE OF A LAYOUT ?
PUROSE OF A LAYOUT -
- Layout gives information of placement of fixture and robot on a station.
- It provides information of working area of a robot. The working area is called the swept area. It tell us the reacabilty of a robot .
- The circle around the robot shows us the swept area.
- It tells us about the space constraint the place has.
Layout provides information on the following points.
- Flow of parts - It tell us the movement of part from from station to another.
- Station pitch - It is the distance between two stations.The layout show shows these distance.
- Robot stations - It gives placed of robot in space as shows in the layout diagram.
- Acessories stations - It gives information of tool changer and tip dressor( tool used to sharpen the tip of weld gun) that are placed on a station
- Sub assembly links - It gives information of links of sub assemblies forming a finl assembly.
- It provides information on loading and loading sequence and it also tells us about the platform height.
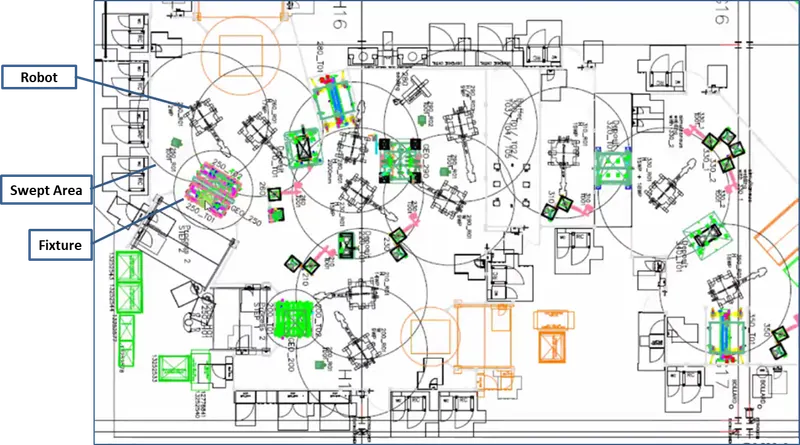
FIG - LAYOUT
6. WHAT IS ERGO DATA ?
Ergo Data
- Ergo data is basically involved well manual operators are involved, and every company has different types of standards for aggregate data, so we'll be getting that particular input from the customer so these are the standards that we follow So, this kind of Ergo data we get from the customer.
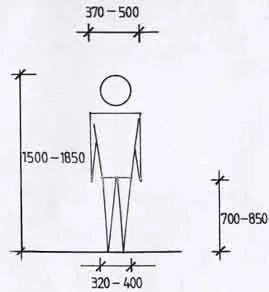
- Ergonomics refers to the study of human behavior and movements.
- Ergo data provides information of loading height, working safety zone of the operator, etc.
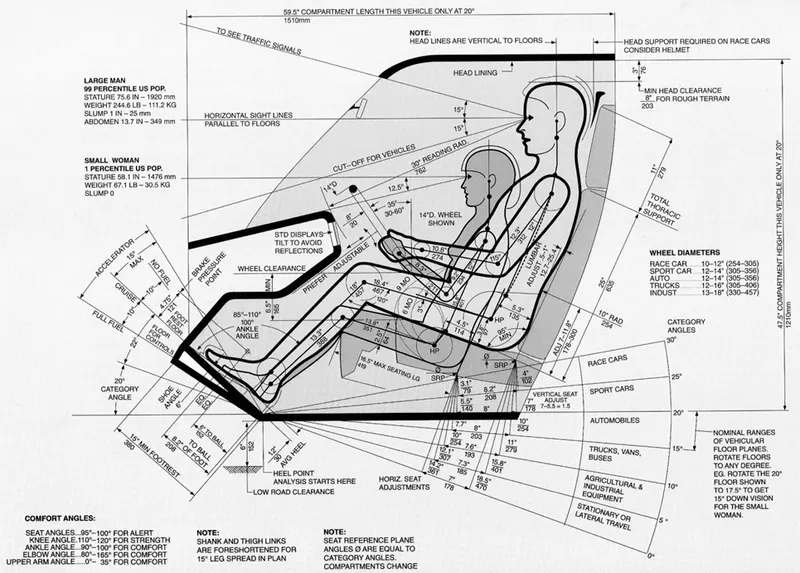
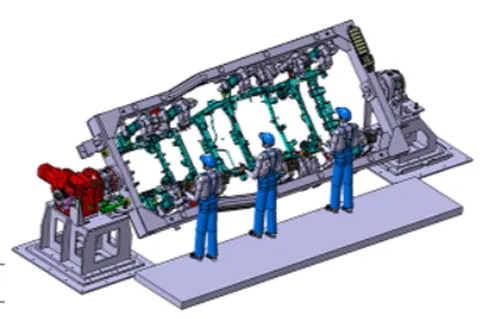
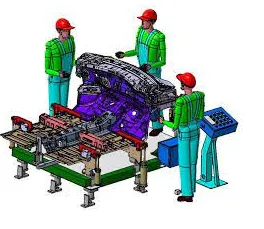
- Ergo data is basically where is given when a manual operation is required. So this import will be given in regards to how their standards of Ergo data so this is one of the standards of the country that they follow for an ERGO data so height and a minimum height of the session we mentioned here, and also the distance, which is required for the operator from the fixture design except.
- So this is very important as images to the study of human behavior and moments, and your data provides information of loading height working safety zone and operation. So it also gives you the safety zone of a particular man operator. So, how much distance is supposed to be from the weld gun?
- The heights are mentioned because of the operator itself, he should not bend, while doing the operation. It was going to be a strain on his back, the height should not be way too much so that he can't even see what are the other particles because it's gonna be uncomfortable for him and his shoulders are gonna get frayed.
- So this is basically to make the operator as comfortable as possible so that he will be more efficient in doing work and he will not take a lot of time while doing the particular assembly.
- The distance from the operator and the component be 1070 is the particular component and this is the reachability 300 if it is there, and the max reachability of the particular operators is 380, so he doesn't have to stretch his arm to get that particular company if it is 380 it's totally fine. If it is 300 that is also acceptable and 1070 particular components or particular parts location.
- The height of that particular component that is acceptable will be around is the operator's waist size, which is easily accessible for him. Again, the maximum height should be 1500, which is also easily accessible to him, and which is done.
- So this is the schematic example of how the algorithm looks like. Effective economic data or effective ergonomic friendly mixture designers, the better the efficiency of the particular operator to work on it, and the less the time consuming, so it's going to be a very important factor, wherever the manual operator doesn't work.
7. WHAT DO YOU UNDERSTAND BY WELD STUDY ?
WELD STUDY -
- It involves study of weld gun.
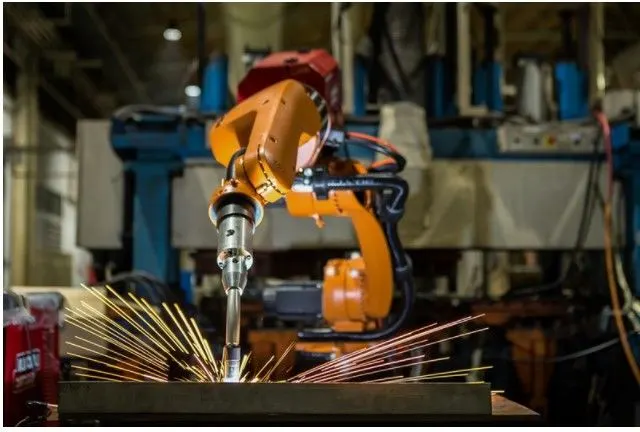
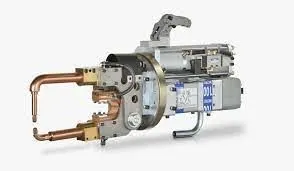
FIG- WELD GUN
- It is a very important input that we get from customer.
- We get the data of the weld gun , no of welds , location of the spots , type of welding from the customer.
- This hepls us alot in design the fixture.
- Generally the weld points are in form of spheres.
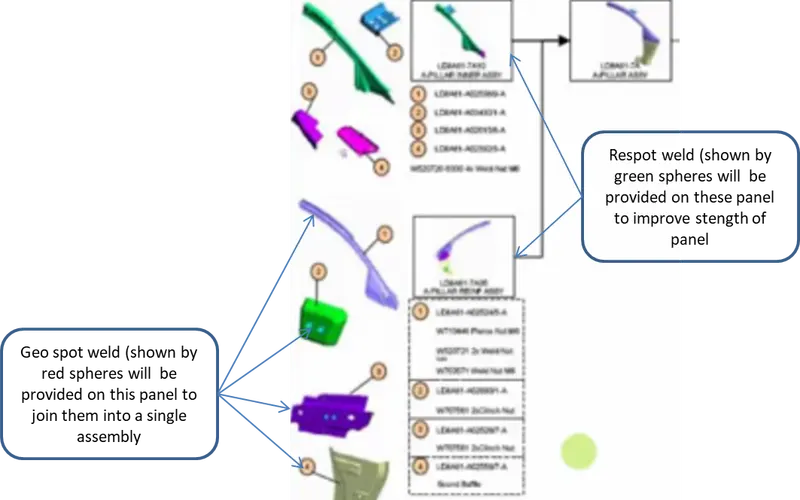
- The red sphere represents the Geo weld spot point and the green sphere represents the Respot weld point.
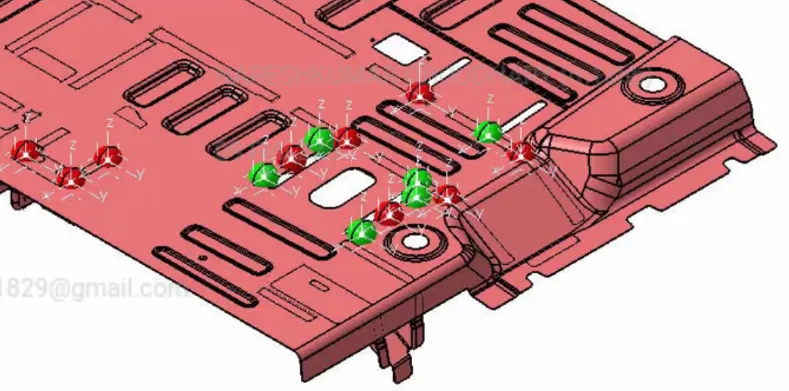
FIG - SHOWS DIFFERENT TYPES OF WELD SPOTS.
The Weld matrix includes the Geo weld points and Respot weld points.
- GEO WELD POINTS -
- They are represented by Red spheres as shown in above fixture.
- These are used in to join sub assembly parts.
- It define the position of the part as per drawing.
2. RESPOT WELD POINTS -
- These weld point increases the strength of the panel.
- They are used to join two sub assemblies together.
- They are represented by Green spheres.
8. WHAT ARE THE CRITERIA FOR PERCENTAGE COMPLETION IN THE DESIGNING STAGE.EXPLAIN IT IN DETAIL?
Percentage of completion criteria
- Percentage completion criteria are basically schedule. What time we can complete the entire process again this is more detailed. So when we are going to complete the entire design, then we're going to move on to simulation on all these subcategories would be considered in percentage completion cafeteria like a probability to when we can complete the entire fixture design.
Percentage Completion Criteria is followed in the designing stages and dispatch stages of welding fixtures.
- 0-25% Input and concept design
- 25-40% Concept approval and simulation
- 40-85% Design freezing and detailing
- 85-100% Check and Final dispatch
- Percentage completion criteria are followed in the design stages and dispatch stages of the welding fixtures.
- For example, where the how much of the task and how much of the project that you have already finished and is it actually lining up with the schedule that you have planned before. And these are the information that we get from particularly a percentage completion criteria.
- Input and concept designing - 0-25%
- In this, they were given four days to design the fixtures that mean we have to complete 25% of the task within four days.
- Concept approval and simulation - 25-40%
- The concept of design is approved here, and the simulation check is done here, which is 25 to 40% of your design is complete in Comcept approval and simulation.
- Design freezing and detailing - 40-85%
- In this process, the design is getting Freeze. That means the design is getting finalized. And the detailing is going to start again. Once the detailing is finished, and the design is also feezed that means you have completed at least 40 to 85% of the task.
- Check and Final dispatch - 85-100%
- This stage is the final stage, Here checking the quality check usage and the final dispatch, which is the output that we are going to give to the customer, which is from 85 to 100%.
8) What are the criteria for percentage completion in the designing stage?
Percentage completion criteria is a time plan / schedule which we define for completion of design. So, when we are going to complete the in entire designing, then we're going to move on to simulation on all these subcategories would be considered in percentage completion criteria like a probability to when we can complete the entire fixture design. The percentage completion criteria is categorized as follows
- 0-25% Input and concept design
- 25-40% Concept approval and simulation
- 40-85% Design freezing and detailing
- 85-100% Check and Final dispatch
Input and concept designing
In this they given four days to design the fixtures that means we have to complete 25% of the task within four days.
Concept approval and simulation
The concept of design is approved here, and the simulation check is done here, which is 25 to 40% of your design is complete in Concept approval and simulation.
Design freezing and detailing
In this process the design gets finalized. And the detailing is going to start again. Once the detailing is finished, and the design is also feezed that means you have completed at least 40 to 85% of task.
Check and Final dispatch
In this stage this is final stage, Here checking the quality check usage and the final dispatch, which is the output that we are going to give to the customer, which is from 85 to 100%.
9) Brief about "Output" in design?
In BIW fixture design or any industry. We don't only just design a particular component and just give the CAD file to the customer. We have to submit a lot of documents like 3d documents, 2d documents which details the part and other factors as well, like bill of material and other documents and the standards followed etc.
To be specific outputs in design should
- a) meet the input requirements for design and development,
- b) provide appropriate information for purchasing, production, and for service provision
- c) contain or reference product acceptance criteria, and
- d) specify the characteristics of the product that are essential for its safe and proper use.
The basic output are 3D models and the 2D drawing of the tools
1.Unitized Tools
In the unitized tools testing requires two types of drawing sheet, which is one key sheet and layout sheet. These sheets are an index of units and placements on the tool base. Layout sheet is a detailed drawing of that particular tool which shows details of components and how and where it is to be placed. Key sheet shows the placement and the location of that particular tool on the tool base where exactly the tool is placed. And what is his exact position in a particular place.
2.Non-Unitized Tools
Non unitized tools are basically tools like Stands and tool changers where you don't need key sheet. Tools that can stand alone and can be detailed completely on a layout. We can use to layout sheet and complete the entire documentation of the particular component.
10) What do you understand by structuring a design tree ? How does it reduce errors during the design process?
ANS 10) Structuring a design tree implies to a process where all the assemblies & parts are named in a specific standard. Different customers have their different set of standards to structure a design tree.
- It is an important process which helps to identify a specific part or assembly as to which project, tool or unit, it
- This helps us to avoid the error during design study, manufacturing, assembly, inspection etc.
- If the parts or assemblies are not properly or the design tree is not structure properly, it will create confusion to understand the design & may create major possibilities of making an error.
- Naming of a fixture or a unit or a part, the information as to which project or zone or a assembly do they belong.
- It has help us to identify the quantity of items of same type or different types are being used in assembly.
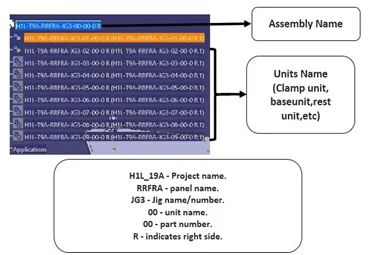
Under the product there are main assemblies, sub-assemblies , child part , standard parts etc. these all parts are provided with specific no. zone etc to identify easily.
QUE 11) What are units? Mention 5 types of units.
ANS 11) A unit is a device that has specified function, specially one forming part of a complex mechanism.
- The BIW fixture is the assembly of different units which are designed to fulfill different purpose.
- The unit have the specified function like resting the panel, clamping the part, locating the part etc.
- According to the 3-2-1 principle of fixture design the units are designed to locate & clamp the car panel to its specified position in fixture while operation is going on.
In the following the different units are showed by different color
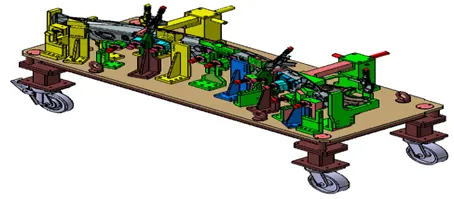
-following are the typical types of units used in BIW fixture design,
1) Fixed pin unit- It is non movable locating unit used for proper location of the part.
2) Retract pin unit- It is movable locating unit.
3) Rough locator unit- It roughly guides the operator for locating the part.
4) Rest unit- The panel is rest on this unit.
5) Base unit- It is the unit on which all other units are mounted
12) Describe Fixed Pin units & their purpose?
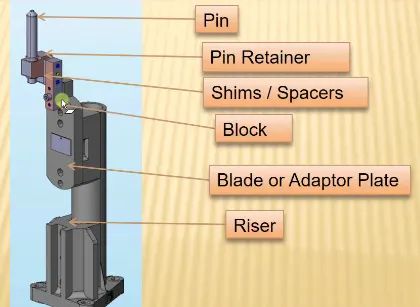
Image 12.0: Fixed pin unit
Fixed pin unit consist of riser, blade, block, shims or spacer, pin retainer & pin. Riser is the standard part which is used to rise up the height of the while unit. Blades are plates mounted on the riser. Other parts like cylinder, arms etc. are mounted on the blade. Shims are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stack up tolerance which reflects at the panel holding part called Mylars. In fixed pin shims are used to adjust to translational motions. Pin retainer will support the pin & the locating pin which restricts movement of the car panel.
Purpose of fixed pin unit:
- Fixed pin unit is a unit designed to locate the car panel using pin.
- The fixed pin unit is the part of the 3-2-1 principle. It restricts 6 degrees of freedom of the car panel.
- It is necessary to have 2 pins to locate car panel. one pin must arrest 4 way (4 translational) & other must arrest 2 way (2 rotational) of a car panel.
13) What are the different parts of a fixed unit?
Fixed unit consist of riser, blade, block, shims or spacer, pin retainer & pin.
1) Riser: Riser is the standard part which is used to rise up the height of the whole unit. Generally, risers are either made of plate fabrication or plate and tube welding together or from single gas cut plate.
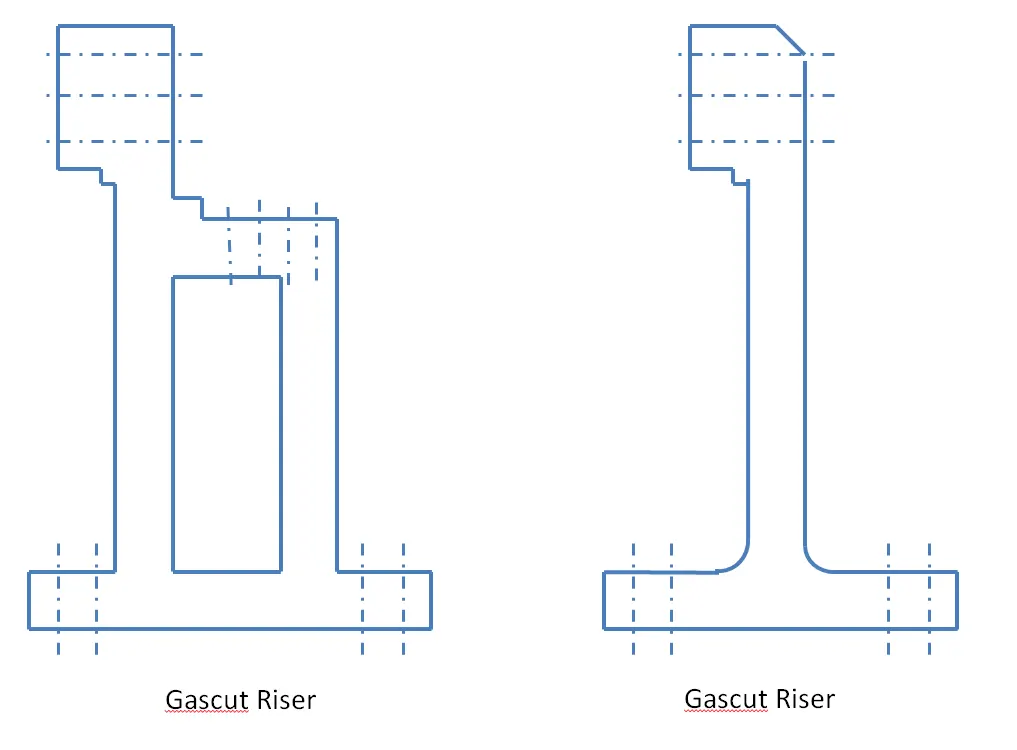
Image 13.0: Riser
2) Blades: These are plates mounted on the riser. Other parts like cylinder, arms etc. are mounted on the blade.
3) Block: Blocks can be machined to any desired fixture component. Because they come as a blank block, the possibilities are endless. Adding new tap holes or grinding down to your specifications are quick and simple.
3) Shims: These are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm etc. These will compensate the stack up tolerance which reflects at the panel holding part called Mylars. We give tolerance to all the parts of the fixture. Due to this tolerance the Mylars will either lift up or goes down from its defined position. If the Mylars goes down from the defined height it will make impression or dent on the panel. If the Mylars lift up then there will be a distortion due to welding stress. To adjust the Mylars At its defined position we use shims so the panel won't deformed & also don’t get any impression on it.
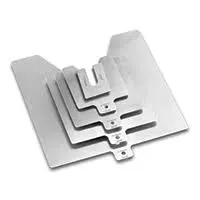
Image 13.1: shims
4) Pin retainer: It will support the pin.
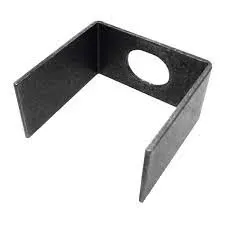
Image 13.2: Pin retainer
5) Locating Pin: Typically, locating pins are used for controlled, fine tolerance positioning of a work piece. For example, a pallet that is moved along one axis, where the drive mechanism is not accurate and stable enough to place it in a position sufficiently accurate to execute a particular process, the use of locating pins may be the best solution. The Diamond Shape is a critical feature that helps with machining inaccuracies and smoother locating operation. When two round head pins are installed onto one plate, the distance between two mounting holes must be extremely precise and even then, the work piece will not be placed on the base as easily as it would with the use of a diamond shape pin.
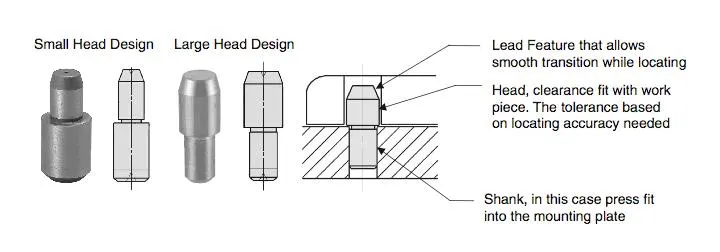
Image 13.3: locating pin
14)What is the purpose of making a Rest unit & describe its parts?
Rest unit:
Rest unit is unit designed to support car panel using Myler/ NC block/ rest component is rested only, no upper clamp or force applied there. It is the simplest unit to design because it has fewer parts to design & the purpose is only resting of the car panel.
Because of the simplicity the rest unit is combined with other unit to reduce the cost of the overall project.
It can be combined with clamp unit to clamp as well as to rest the car panel. It can be combined with locating unit to locate as well as to rest the car panel. Also locating, clamping & Test unit can be combined together in one unit to reduce cost.
There is no cylinder attached to it.It has rest Mylar, blade and riser & below is different parts of rest unit.Rest unit is also divided into simple support unit, multiple support units & retractable support unit.
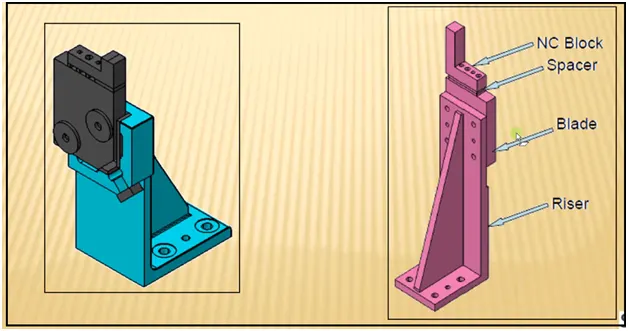
The different parts of a Rest unit are:
- NC bolcks/Mylars
- Spacers
- Blade
- Riser
NC blocks/Mylars:
Mylars are the part which are holding the panel from top & bottom.It is a jaw type,during welding it wont deforms from its position.It is also known as fingers.It wont allow the deformation of the part due to welding stresses.
Mylars are of two types,they are
- Clamping mylars
- Resting mylars
Only resting mylars are seen in resting unit.The panel which rests on the part is nown as resting mylars.
Risers:
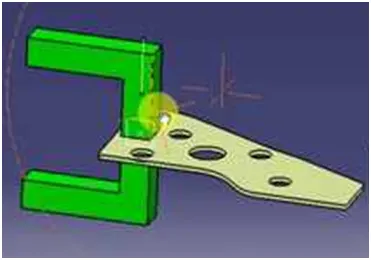
Riser is a structure generally used to mount the toggle clamp and rest, clamp mylars and location pin.
It is not necessary to have one riser where all the parts of clamp or rest or location units are mounted.
Generally risers are either made of plate fabrication or plate and tube welding together or from single gas cut plate.
These are generally manufactured to give height to the assembly.
Spacers/Shims:
Metal shims are used to finely adjust the location of how the fixture holds the product so that it is welded together within the dimensions set for the product to work well.
A pack of thin metal shim is placed between two components in the fixture. The first component is fixed in place and the second component is attached to the first component with the pack of shims in between. Removing one shim or adding one shim slightly adjusts the location of the second component. This is important to manufacturers who want to have their product’s parts assemble easily after being welded.
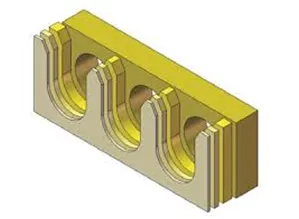
Blade:
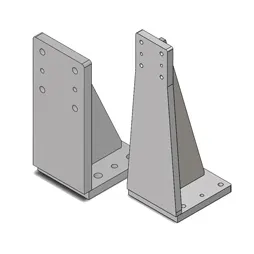
Blades are the plates attached to the riser.Other parts like cylinder,arms etc are mounted on the blade.Chamfer is given here to strengthen the blade.
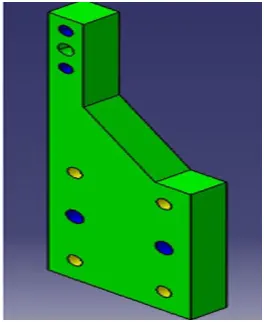
Hence ,these are the different parts in a rest unit.
15)What are the basic fundamentals to design a Sensor unit?
Sensor unit:
A sensor is a device that measures physical input from its environment and converts it into data that can be interpreted by either a human or a machine. Most sensors are electronic (the data is converted into electronic data), but some are more simple, such as a glass thermometer, which presents visual data. People use sensors to measure temperature, gauge distance, detect smoke, regulate pressure and a myriad of other uses.
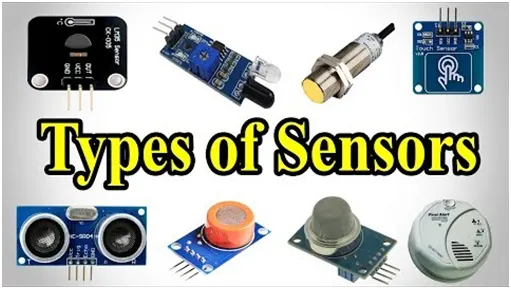
Types of Sensors used in general are:
- Proximity sensors
- Photo electric sensors
- Laser sensors
Proximity sensors:
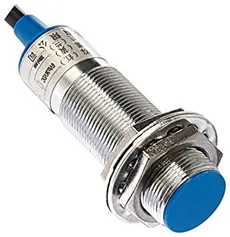
A proximity sensor is a non-contact sensor that detects the presence of an object when the target enters the sensor’s field. Depending on the type of proximity sensor, sound, light, infrared radiation (IR), or electromagnetic fields may be utilized by the sensor to detect a target. Proximity sensors are used in phones, recycling plants, self-driving cars, anti-aircraft systems, and assembly lines. There are many types of proximity sensors, and they each sense targets in distinct ways. The two most commonly used proximity sensors are the inductive proximity sensor and the capacitive proximity sensor.
An inductive proximity sensor can only detect metal targets. This is because the sensor utilizes an electromagnetic field. When a metal target enters the electromagnetic field, the inductive characteristics of the metal change the field’s properties, thereby alerting the proximity sensor of the presence of a metallic target. Depending on how inductive the metal is, the target can be detected at either a greater or shorter distance.
Capacitive proximity sensors, on the other hand, are not limited to metallic targets. These proximity sensors are capable of detecting anything that can carry an electrical charge. Capacitive sensors are commonly used in liquid-level detection.
Photoelectric Sensors:
Photoelectric Sensors detect objects, changes in surface conditions, and other items through a variety of optical properties.A Photoelectric Sensor consists primarily of an Emitter for emitting light and a Receiver for receiving light. When emitted light is interrupted or reflected by the sensing object, it changes the amount of light that arrives at the Receiver. The Receiver detects this change and converts it to an electrical output. The light source for the majority of Photoelectric Sensors is infrared or visible light (generally red, or green/blue for identifying colors).
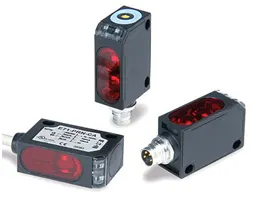
Laser Sensors: These laser distance sensors use a focused, coherent light to measure distance to a target object. In factory automation applications, the target is usually a product or a machine element. They detect any solid object and produce an output proportional to the measured distance—independent of material, color and brightness. The high-resolution output provided by laser distance sensors is used to provide position or displacement, usually to the input of some type of industrial controller, such as PLC. The output signal is often highly accurate, and it includes temperature compensation to enhance stability. There are several types of laser distance sensors including diffuse, background suppression and retro reflective. These sensors use CMOS or transit time technologies, providing accurate distance measurements. Laser light must be focused, and it must stay narrow over a great distance and at a narrow spectrum (color of light). The emitted light can then be triangulated or pulsed, with each pulse return measured to create distance readings.
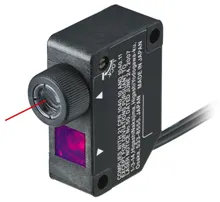
Fundamentals of Sensor Design:
- Every single loose panel, which are being welded in a tool should be sensed.
- Each panel should be sensed by one or two sensors depending on the size of the panel preferred to be in diagonally opposite ends of the panel.
- If a component is really small, we need not use two or three sensors for that you can use one sensor to detect the particular panel.
- If the panel is really big, we will use two sensors in opposite directions to sense the panel.
- So every sensor should be mounted in three directional adjustable ways in general.
- Sensor manufacturers are IFM, Peperl-Fuchs, OMRON etc
Q-16 What is rough locator unit ? What are the fundamental to consider while designing it.
- Rough locators helps to locate workpieces in the automation process. Locating refers to the desired location where you want the workpiece to be when it is getting worked on either by a person, team, or robot.It is a device to establish and maintain position of a part in a jig or fixture.
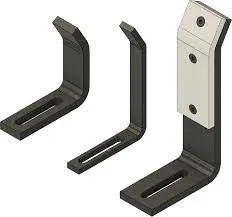
The basic fundamental to consider while designing :
- Rough locators should be placed at edges of the car panel which has to guide.
- Rough locators should be placed at the same angle of the car panel edge with min. distance of 2-5 mm from the edge of the car panel.
- Rough locators should guide the panels in pin assembly direction in general.
- The slot should be in direction of car part only.
Q-17 What is a base unit ? Describe its parts.
- A base unit is the unit designed to mount all the other units(Clamp unit, Pin unit, rest unit etc.) of the tool, also other parts necessary for a tool like pneumatic valve box, trunking cable path will also be mounted on to a base unit.
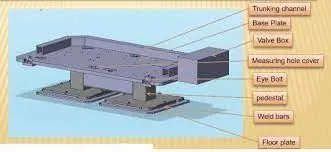
Parts of base unit :
1. Valve box
2. Truncking channel.
3. Measuring hole cover.
4. Eyebolt
5. Pedestal
6. Floor plates.
1. Valve box.
- A valve box is a box that supplies air to all the pneumatic cylinders assembled in the fixture valve box consists of one solenoid valve with one inlet & one outlet. The outlet in the solenoid is used to
supplies air to the pneumatic cylinders from the valve box whereas , the inlet in the solenoid valve is used to collect the air from pneumatic cylinders to the valve box.
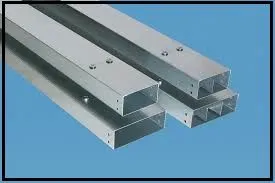
2. Truncking channel.
- Tuncking channel is kind of cable duct. Which helps to guide & protect the wiring / tubes used in the fixture.
3. Measuring hole cover.
- In the measuring hole cover the co-ordinates points are engraved on it. The hole which mentions the co-ordinates gives the position & placements of the particular units.
- The measuring hole helps in CMM & OC inspection.
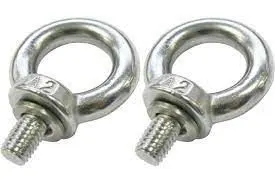
4. Eyebolt.
- The eyebolt is bolt with loop at one end , they are firmly attach a securing eye to structure so that ropes or cable may then be tied to it for lifting purpose.
- Eyebolt is used to drag or lift the base unit while relocating.
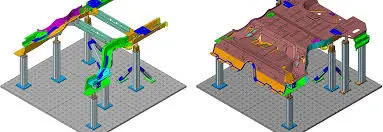
5. Pedestal : Pedestal is a stand like structure where the entire unit of the base will be mounted.
6. Floorplates.
- Floor plates are used to mount the entire base unit with floor.
- also it helps to achieve flatness for the future.
Q-18 What is dump unit & what are its function ?
- Dump unit is the complex unit to design due to space constains there is less space avilable & have to adjust all the parts in available space. It consist of dump cylinder to perform the operation of clamping & unclamping car panel.
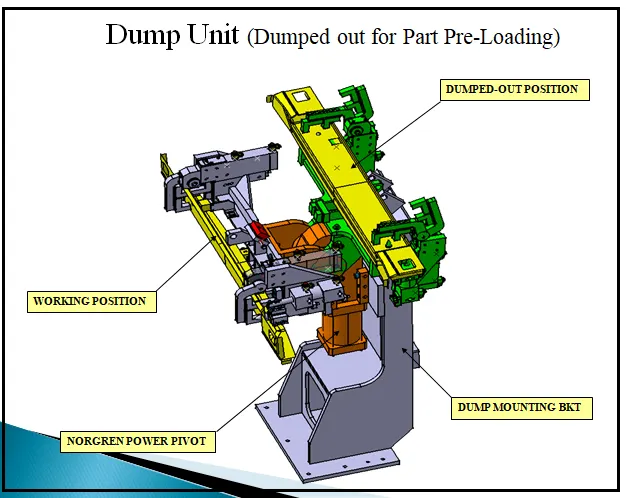
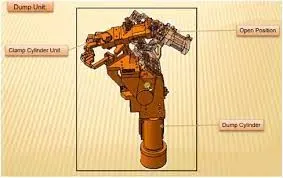
Function of dump unit :
- To ensure proper resting of the panel being welded and to restrict its motion. To ensure there are is no rotation in the panel and to fix it either by pins or side blocks or magnets.
19)What are slide units? Mention where slide units are commonly used?
Slide units:
Slide units are positioning units, which are used to position the car part or panel, units, weld gun, robots for further operations.
Slide units may be classified into two types based on the type of guide ways. They are,
- Hardened guide way.
- LM guide way
Slide units may further classified into three types based on the prime mover. They are,
- Manual slides
- Hydraulic/pneumatic slides.
- CNC slides
It may be further classified depending on the application as
- horizontal slide unit
- Vertical slide unit
- Angular slide unit
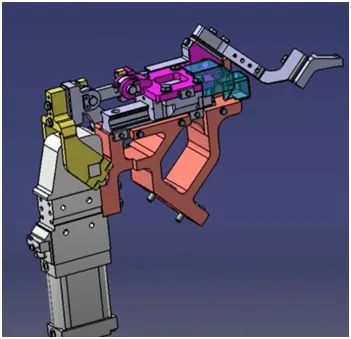
Basic fundamentals of slide unit design:
- Reverse stroke 10mm to be considered in both forward & retracted condition.
- Cylinder & LM guides to be validate for load & stroke.
- Master guide way should be constrained & the subsidiary guide way to be free.
- Mechanical hard stop to be considered for both extended & retracted condition.
- Shock absorber should be used for both extended & retracted condition to reduce impact load.
- Slide to be locked/clamped in the working position.
- Slide to be locked with a safety pin in the retracted position during transportation,
- The two end limits to be sensed externally by a proximity switch
- The design should be checked for screw accessibility, ease of assembly, machinability of parts.
- The LM guide & rails are integral assemblies and should not be separated at any cost.
- LM guide ways to be lubricated for long life.
Hence these are slide units