Week 12 Challenge
AIM:
To create the core-cavity blocks and all the other parts necessary for molding the plastic component.
DESCRIPTION:
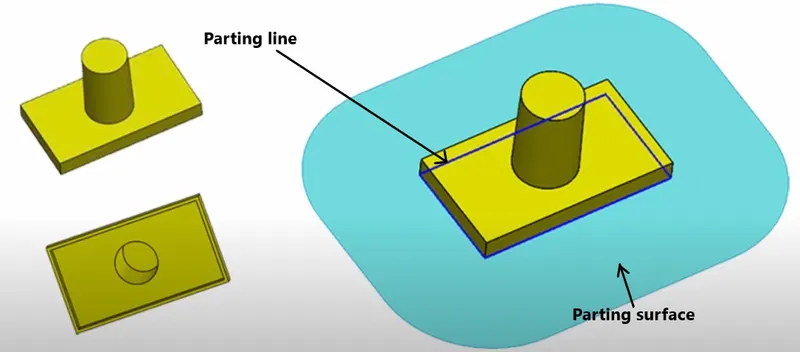
Parting line-
A 'parting line' is the line of separation on the plastic part where the two halves of the plastic injection mold meet.
Parting surface-
A parting surface is a surface that separates the mold block into two parts – the core and the cavity.
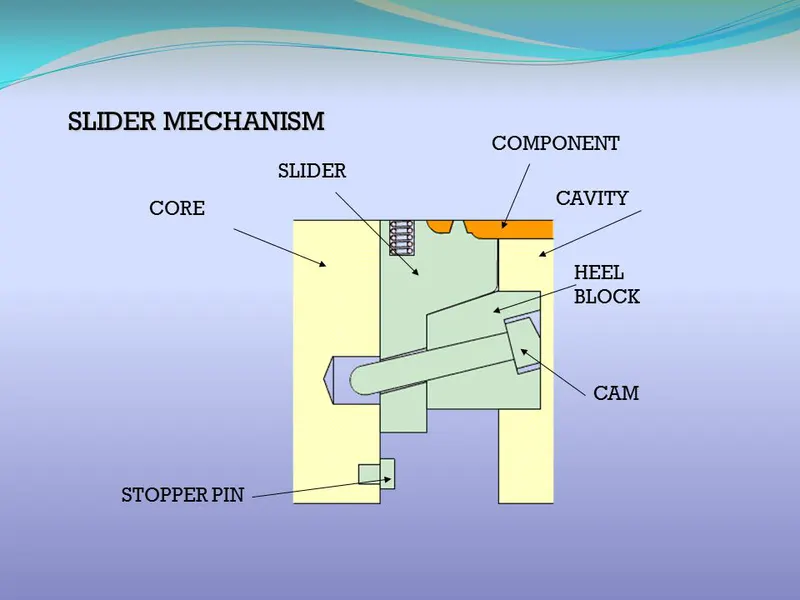
Sliders and Cams-
Sliders and cams are moving parts within the mold that allow or restrict access to particular areas within the tooling (and thus facilitate the desired shape of the part). The use of sliders or cams can facilitate ejection of certain areas of plastic that might otherwise be trapped in the tooling.
Inserts-
It is a separate block that would be inserted in the main block to form the complete core block. Some feature in the block cannot be cut using the current tool available. So we use inserts.
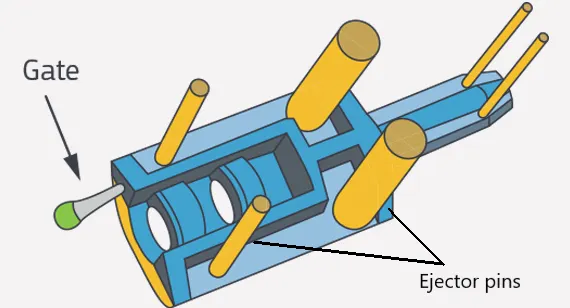
Ejector pins-
Ejector pins apply a force to eject a part from the mold, and in some cases can leave marks. Once the mold is opened, the pins extend into the mold cavity, push the part out, and then retract, allowing the mold to close and be refilled.
Sprue, Gate and runners-
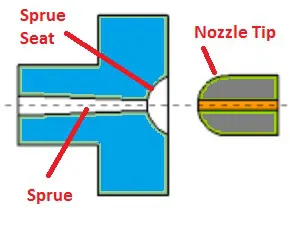
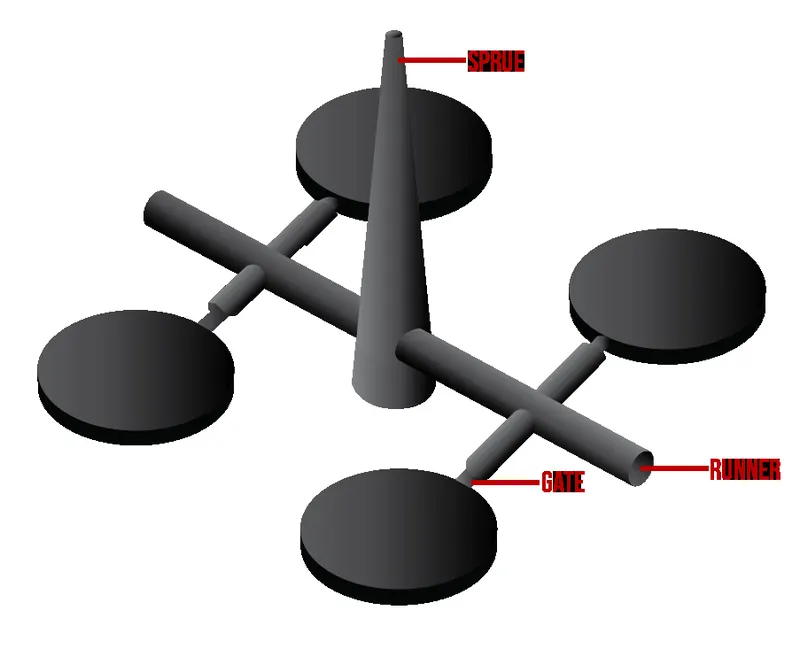
Sprue-
This is the contact point between the machine and the mold. The sprue has a concave spherical seat where the molding machine nozzle tips seats off.
Runner-
The plastic flows from the sprue into the runner system. The runner is the channel that feeds directly into the gate of each part.
Gate-
The plastic flows from the sprue into the runner system. The runner is the channel that feeds directly into the gate of each part.
Cooling channel-
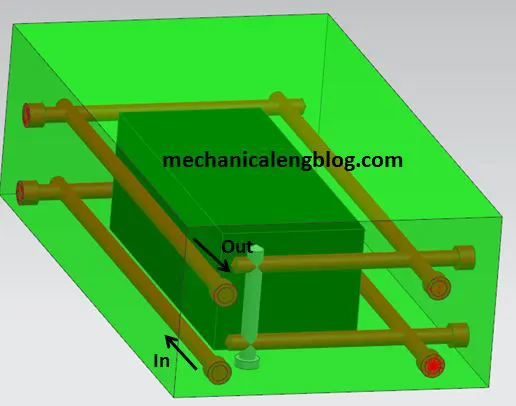
cooling channel is a cooling passageway which follows the shape or profile of the mould core or cavity to perform rapid uniform cooling process for injection moulding or blow moulding processes.
Air vents-
Vents are cuts within the mold steel that allows air to escape. Air inside of the mold must be allowed to escape so that the plastic can fill the entire space. If air fills the cavity then it would lead to defect in the component.
PROCEDURE:
Plastic knob-
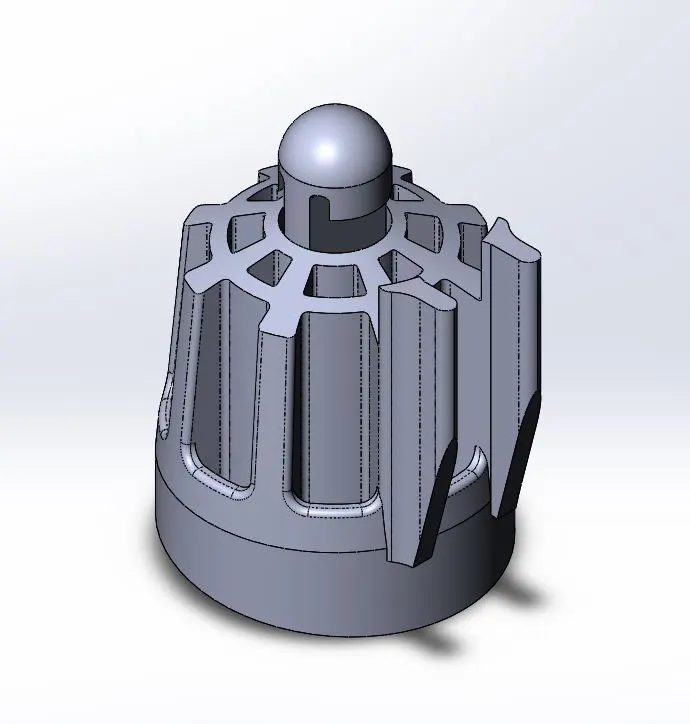
Steps for making the core and cavity block-
Step 1-
Decide the tooling direction and then do the draft analysis. Usually the draft angle of 0.5º is given.
Then decide the core and cavity side.
While deciding the core and cavity side we also see the number of ribs or any feature on both side and the side which has more number of features is taken as the core side and the other side and the cavity side.
This is done because the core side has ejector pins, so we eject the component easily without it getting stuck.
Step 2-
Use the scale command to increase the size of the model to account for the shrinkage.
Here the material used is ABS and the shrinkage percentage for ABS is 0.6%
So, we will make the model 1.006 times bigger than the model given to us.
Step 3-
We need to close or fill the surface for creating the core and cavity block. Use the shut off surface command to fill the holes. For some holes shutoff surfaces are created properly. The surfaces which are not formed properly there select the ‘no fill’ option So here use the loft command to create the surface.
Step 4-
Use the parting line command to create the line on the core and cavity separation.
Step 5-
Create a parting surface. For creating a parting surface first split the edges so that ruled surface command can be used properly. Then draw a sketch on the top plane to that a specific direction can be given. Use the ruled surface command to creating the parting surface.
Step 6-
Create the core and cavity surface. Use the move/copy bodies tools to copy the parting surface and the lofted surfaces created for the shutoff surface. Then knit one of the surfaces with the surface body for the core and the other surface with the surface body for the cavity. By doing this two surface gets created for the core and cavity mold.
Step 7-
Go to the assembly workbench and insert the part we created and make new part for the core and cavity,
Whenever we have a part with 3D profile, we don’t make the entire mold block with 3D profile. We only the the 3D profile upto some distance near the main component and the rest of the block will have a 2D profile.
The width of the mold depends on the size of the ejector plates. Besides the ejector plate there is also the spacer blocks the standard size of the spacer block is 45mm. Also we add 50mm more in the width for the bottom support. Considering the sprue at the centre the mould is designed.
The length should be atleast 50 mm distance from the component.
For 3D profile the distance between the component and the block should be atleast 30mm. The length of the block should always start from the sprue position which is at the centre.
Use the extrude command and then use the cut with surface command to create the core and cavity block separately.
The thickness of the block depends upon the cooling channels. The distance between the cooling channel and core block is kept at 40mm. The thickness is considered from the top most part of the block to the bottom flat base of the block.
Reliefs are created on the core and cavity blocks using the move surface command so that there wouldn’t be any steel to steel rubbing at 90º
Step 8-
Inspect the region in the core block which and see which feature cannot be cut using the tool in the core block. Use the sketch command and sketch around that and then make a reference plane. When we have inserts on the block then keep atleast 40mm distance between the insert and base of the block. Use the split command so separate it from the main core body.
Step 9-
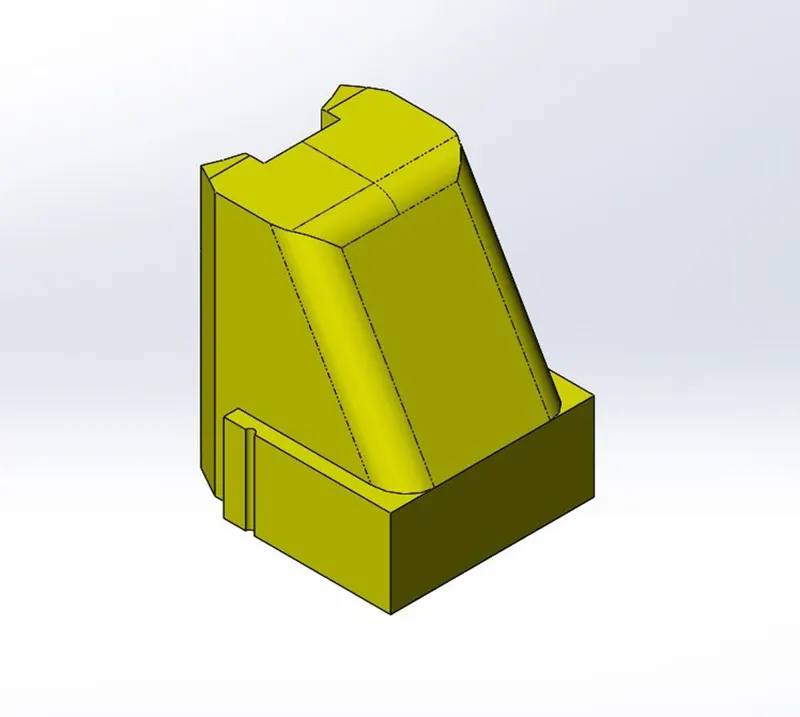
In this step, draw a sketch on the top most surface for the slider and then make a reference plane so that we could split a solid body for the slider. Because of the split, two new under cuts are created. Now to remove these undercuts, we draw a new sketch on top according to which the area of the undercut would be avoided and make a new reference plane and split it solid body. Now we get a total of 4 solid bodies, one is the slider, the other is the core and the remaining two we would consider that as inserts since they are small solid bodies.
Step 10-
In this step we make the guide rails for the slider to move. The guide rail should have enough width to fit the washer. Create the guide rail in the core block using extrude command. Now since the guide rail was made in the core block, fill cavity for the guide rail in the cavity block.
Step 11-
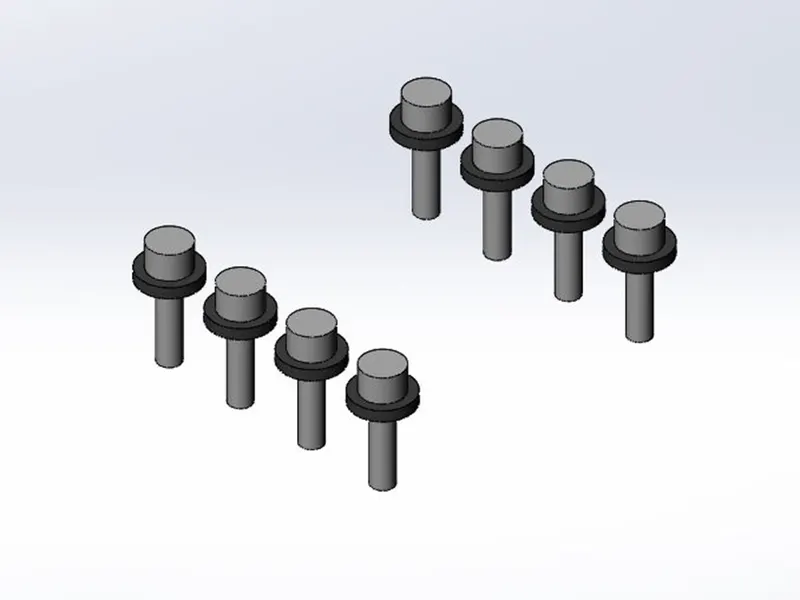
In the assembly file create a new part for the washers. Draw the sketch for the washer with diameter of 16mm and then extrude it. Then we create a bolt to and then use sketch driven pattern to copy it along the slider and washers.
Use the hole wizard to create a tapped hole on the core block.
After creating this, edit the cavity block too to create a cavity for the washer and the bolt.
Step 12-
Locking mechanism is created on the core block. Create sketch on the core mold for the locking mechanism and the use the cut extrude command to cut from the core mould. Then travel distance pf the slider is taken as 35mm, so while creating the slot for the slider it then made at a distance of 15mm from the slot in the core.
Step 13-
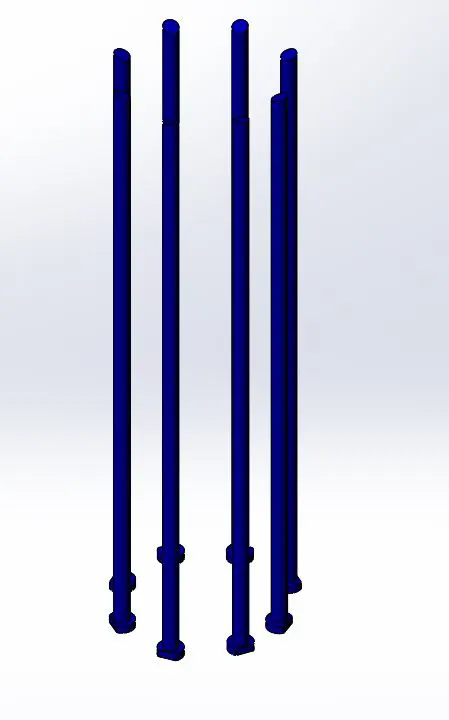
Create the ejectors pins for the mold. With the help of sketch tool draw the sketch for the cut for ejector pins with a diameter of 6mm. Then use extrude cut to cut through the whole mold.
For making the ejector pins offset the sketch surface of the pins to a certain length and extrude it upto the surface where there is a cut for the ejector pins. Then we create a relief for the ejector pins in the core mold using the extrude command.
Since the top of the pin is angled one, this ejector pin is of second type. So the base of the ejector pin is made D shaped. So we sketch and extrude the base in that shape.
Using the bottom face of the pin we make the sketch of the ejector plate of the same length as that of the mold but the with 45mm less from both the side. Then extrude it. In the same way we make ejector plate support and then make a relief for the ejector pin and base in the ejector plate.
Step 14-
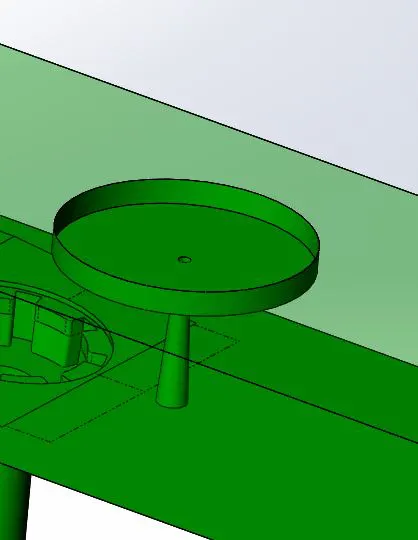
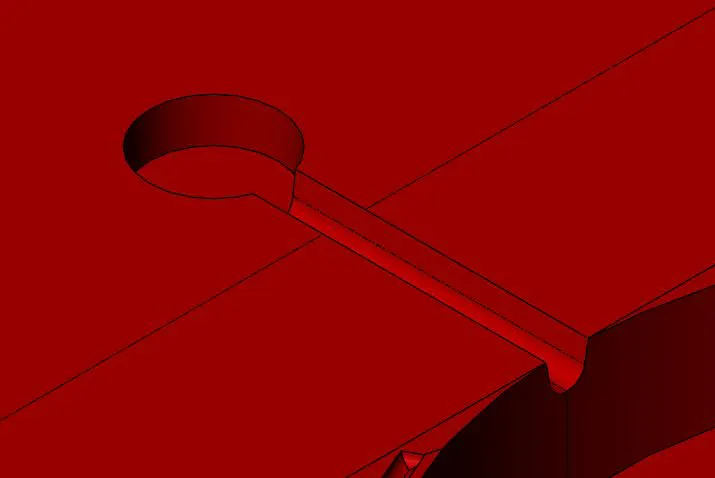
Create a sprue, runner and a gate. First thing is to edit the cavity block and create a sketch a circle at the centre and extrude cut it. This cut is for the proper alignment of the nozzle. Now we make a sprue and make sure that it is tapered and it will extend throughout the surface. A sprue puller is provider in the core block.
Then for the runner we make a line sketch and extrude it 4.5mm thick in the thin feature without merging it with the core block. Give a draft of 10º, then give a fillet in the bottom of 2mm.
Sketch for the gate in the shape of a trapezoid and extrude it to 0.5mm. now for the bottom part of the gate, we give a draft of 40º. Sketch and use the intersection curve command so that the remaining material can be removed using the cut extrude command. Use the fillet tool. Combine the gate and sprue and then with the help if the same combine using the same combine tool select subtract and subtract the gate and runner body from the core mold.
Step15-
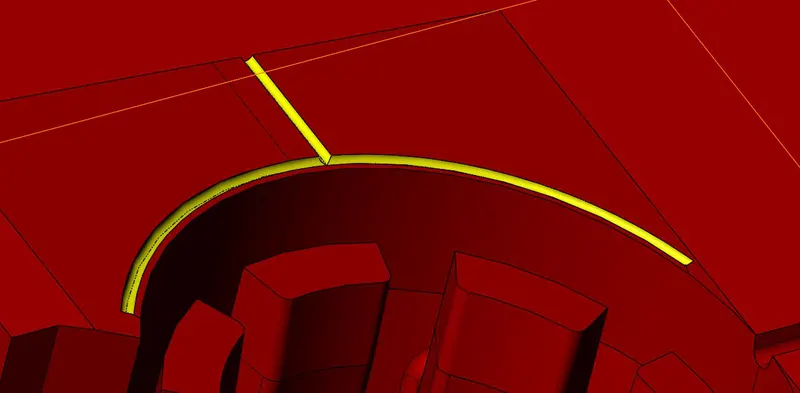
While making the air vent we first sketch and offset the surface from where we want to provide the vent and extrude the line upto a distance on both direction and without merging it with the core body. Then we use the split body command to get the angled surface and then use the move face command and move it to 1mm. then fillet.
Then make another sketch and which joins the part and the vent and then use the same method as above only difference that instead of moving the face upto 1mm. move it upto 0.02mm. Make the line sketch and again repeat the same step and fillet it. Then combine it and then subtract it with the main body.
Step16-
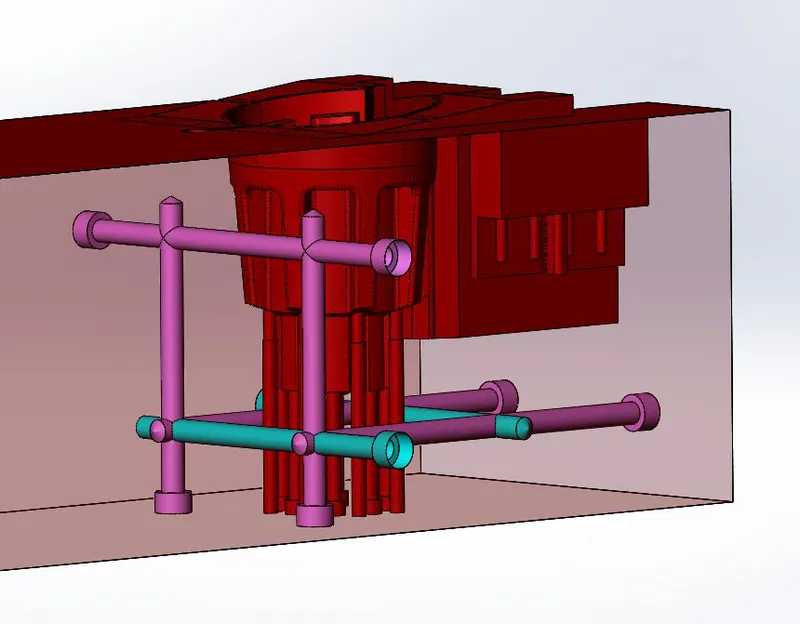
For the colling channel we follow the serial cooling channel since the flow rate is same and it causes uniform cooling. We use the hole wizard command and in that we use the socket head cap screw and then make the channel accordingly.
Result
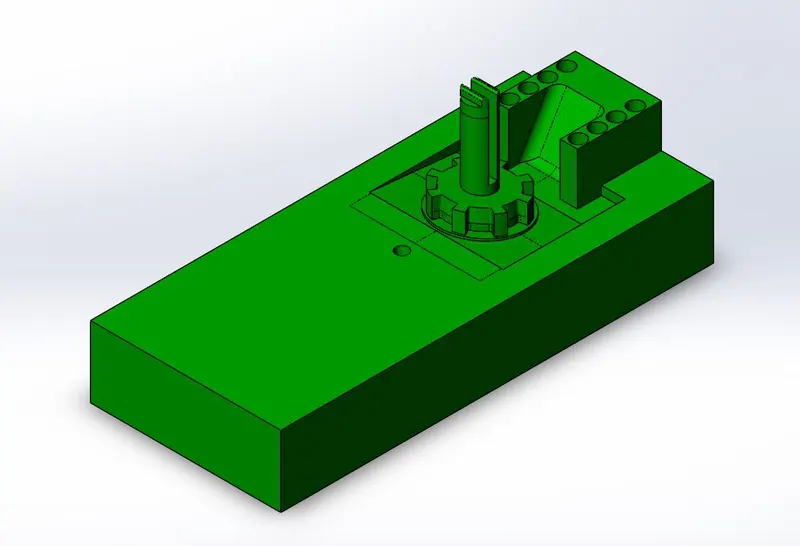
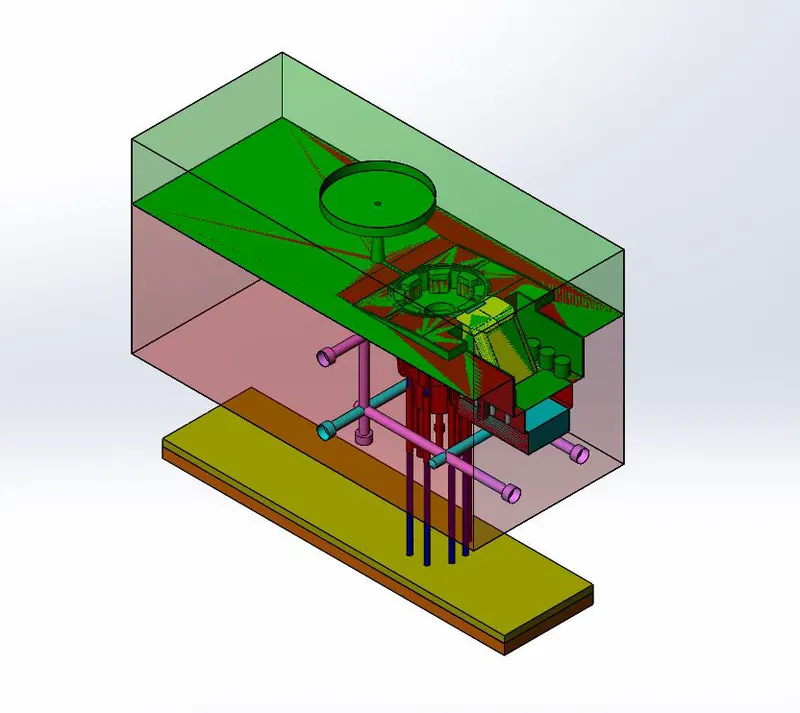
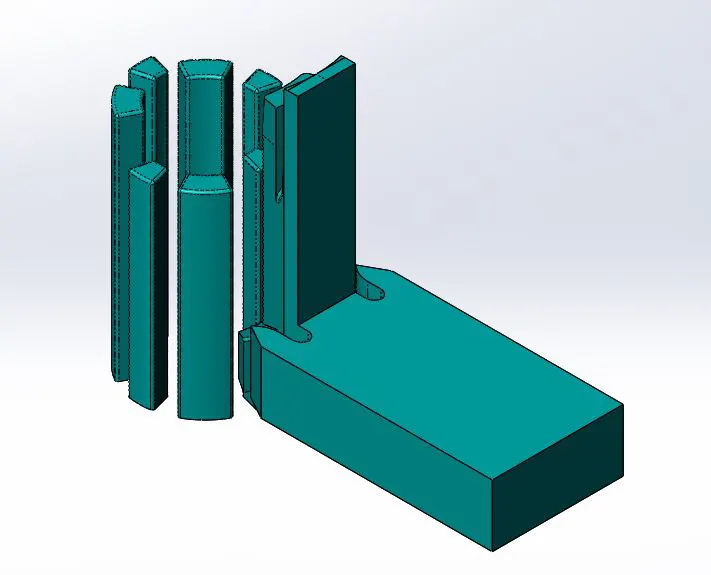
CONCLUSION;
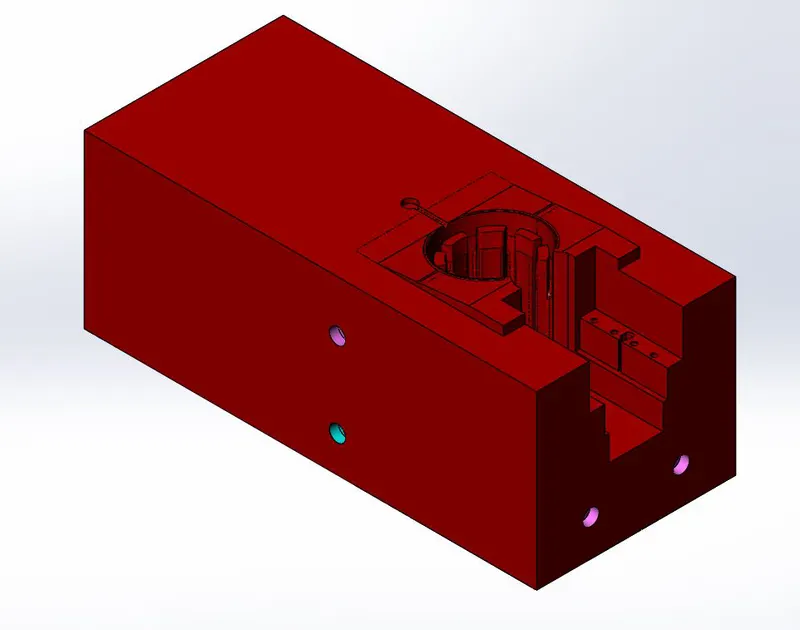
With this we got to learn about the core and cavity block and also about ejector pins, air vents, cooling channels, gate and ruuners and how to create them using solidworks.