Week 1 Spur Gear Challenge
Introduction :-
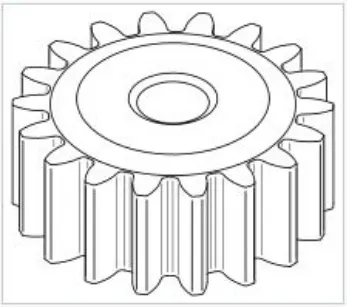
Spur gears or straight-cut gears are the simplest type of gear. They consist of a cylinder or disk with teeth projecting radially.
Though the teeth are not straight-sided (but usually of special form to achieve a constant drive ratio, mainly involute but less commonly cycloidal), the edge of each tooth is straight and aligned parallel to the axis of rotation. These gears mesh together correctly only if fitted to parallel shafts. No axial thrust iscreated by the tooth loads. Spur gears are excellent at moderate speeds but tend to be noisy at high speeds. Spur gear teeth are manufactured by either involute profile or cycloidal profile. Most of the gears are manufactured by involute profile with 20° pressure angle. When two gears are in mesh at one instant there is a chance to mate involute portion with non-involute portion of mating gear. This phenomenon is known as "interference" and occurs when the number of teeth on the smaller of the two meshing gears is less than a required minimum. To avoid interference we can have undercutting, but this is not a suitable solution as undercutting leads to weakening of tooth at its base. In this situation Corrected gears are used. In corrected gears Cutter rack is shifted upwards or downwards.
The spur gears can be classified into two main categories: External and Internal. The gears with teeth cut outside of the cylinder are known as external gears. The gears with teeth cut on the internal side of the cylinder are known as internal gears. An external gear can mesh with an external gear or an internal gear. When two external gears mesh together they rotate in the opposite directions. An internal gear can only mesh with an external gear and the gears rotate in the same direction. Due to the close positioning of shafts internal gear assemblies are more compact then external gear assemblies.
Stress Intensity:
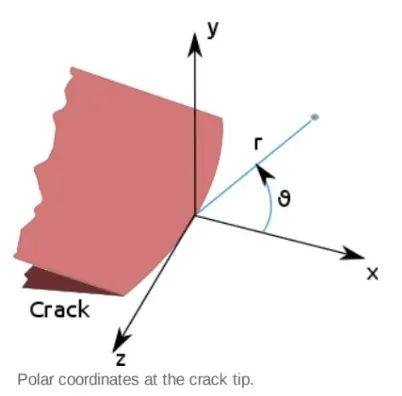
The stress intensity factor,, is used in fracture mechanics to predict the stress state ("stress intensity") near the tip of a crack or notch caused by a remote load or residual stresses.
[1] It is a theoretical construct usually applied to a homogeneous, linear elastic material and is useful for providing a failure criterion for brittle materials, and is a critical technique in the discipline of damage tolerance. The concept can also be applied to materials that exhibit small-scale yielding at a crack tip. The magnitude of stress intensity depends on specimen geometry, the size and location of the crack or notch, and the magnitude and the distribution of loads on the material. It can be written as: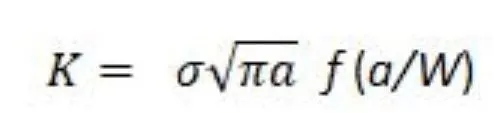
Where, f(a/W) is a specimen geometry dependent function of the crack length, a, and the specimen width, W, and is the applied stress.
Linear elastic theory predicts that the stress distribution 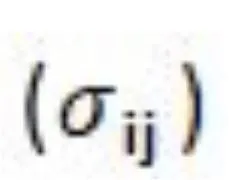 near the crack tip, in polar coordinates
(r,θ) with origin at the crack tip, has the form as: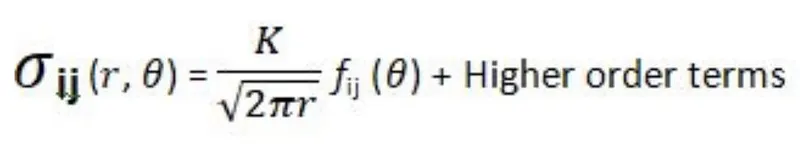
Where is the stress intensity factor (with units of stress length'/2) and fi is a dimensionless quantity that varies with the load an geometry. Theoretically, as goes to 0, the stress
Tij goes to o resulting in a stress singularity. Practically however, this relation breaks down very close to the tip (small) because plasticity typically occurs at stresses exceeding the material's yield strength and the linear elastic solution is no longer applicable. Nonetheless, if the crack-tip plastic zone is small in comparison to the crack length, the asymptotic stress distribution near the crack tip is still applicable.
Stress Intensity Factors for various modes:
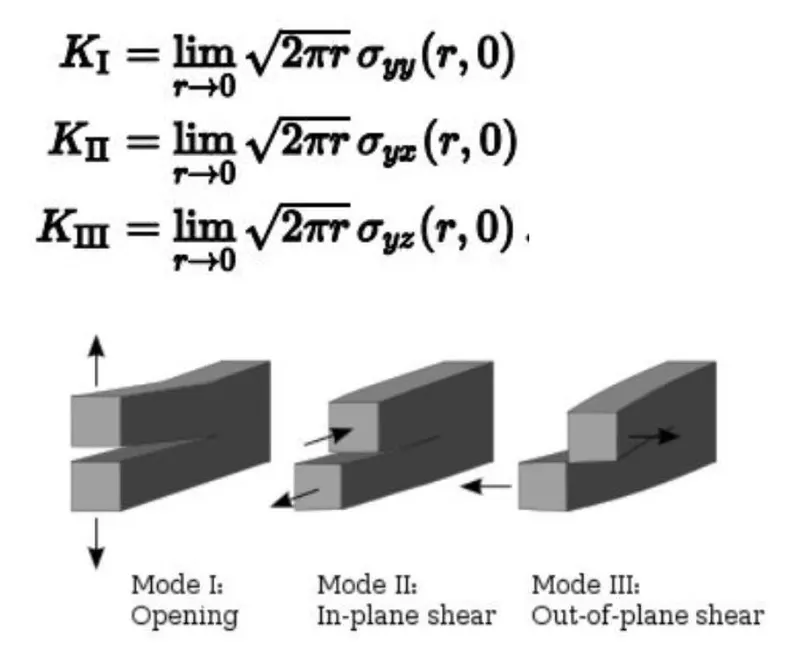
In 1957, G. Irwin found that the stresses around a crack could be expressed in terms of a scaling factor called the stress intensity factor. He found that a crack subjected to any arbitrary loading could be resolved into three types of linearly independent cracking modes. These load types are categorized as Mode I, Il, or Ill as shown in the figure. Mode I is an opening (tensile) mode,
Where the crack surfaces move directly apart. Mode II is a sliding (in-plane shear) mode where the crack surfaces slide over one another in a direction perpendicular to the leading edge of the crack. Mode Ill is a tearing (antiplane shear) mode where the crack surfaces move relative to one
Another and parallel to the leading edge of the crack. Mode I is the most common load type encountered in engineering design.
Different subscripts are used to designate the stress intensity factor for the three different modes. The stress intensity factor for mode I ls designated K and applied to the crack opening mode.
The mode lll stress intensity factor,, applies to the crack sliding mode and The mode Ill stress intensity factor, KIll, applies to the tearing mode. These factors are formally defined as:
Example : Uniform uniaxial stress
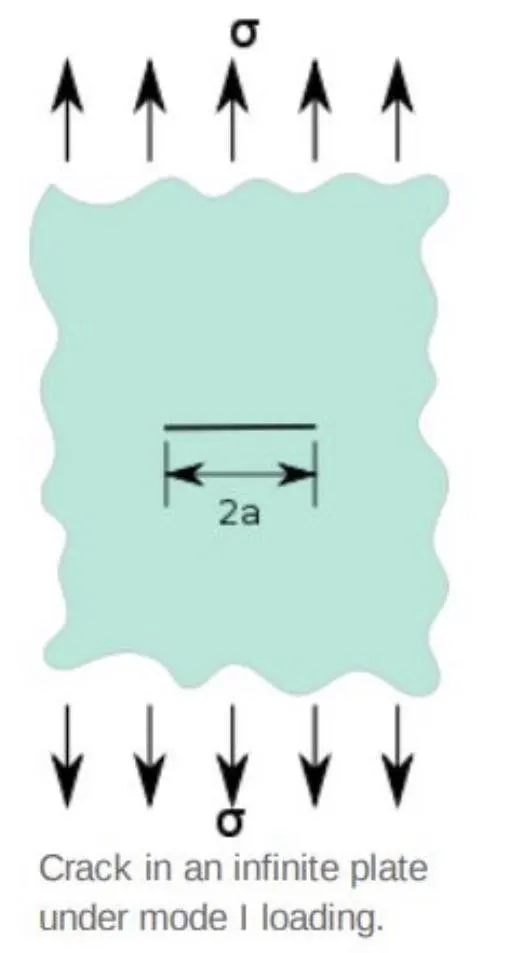
The stress intensity factor for an assumed straight crack of length 2a perpendicular to the
Loading direction, in an infinite plane, having a uniform stress field is
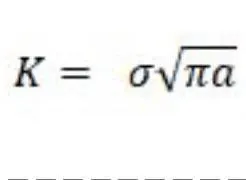
Analysis:
Here we will perform an analysis on a pair of Spur Gears.
We will use different materials for gears and find out the Equivalent stress, Total Deformation and Stress Intensity, where Stress intensity results gives the location of possible
fracture of Gears.
Different Cases of Materials for analysis are as given below:
CASE 1: Cast Iron (Ductile)
CASE_2: Cast_Steel
CASE_3: Cast_Bronze
Geometry:
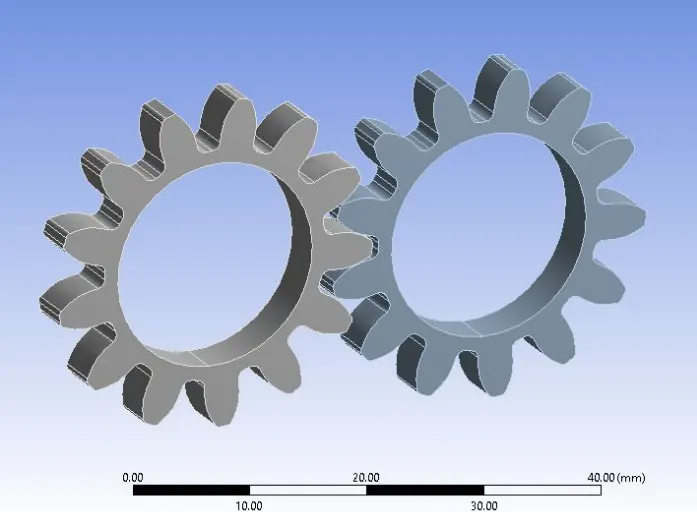
Spur Gear geometry for analysis of all cases is given as below:
Mesh :
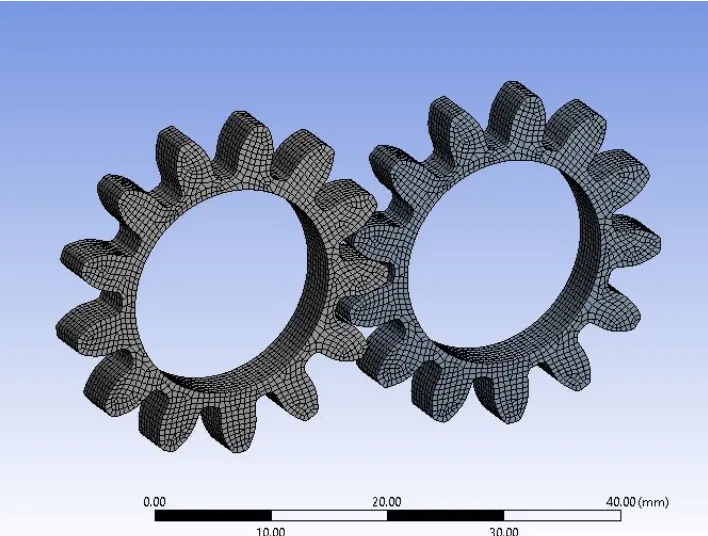
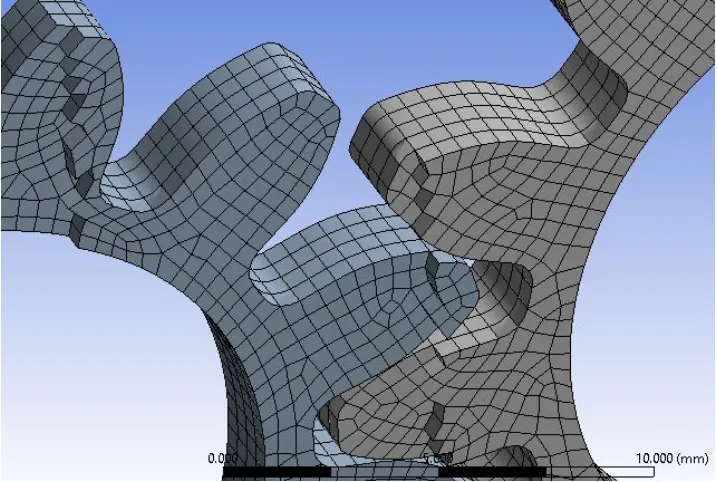
Details :
Element Size: 0.5 mm
No. of Nodes: 86102
No. of Elements: 17232
• We can see in above image that most of the elements are automatically taken as Hexahedral.
Procedure:
• Get Static Structural from Analysis Systems.
• In Engineering Data, select "Granta Design Sample Materials"
• From the Material list, add Material "Cast_Iron (Ductile)", "Cast_Steel" or "Cast Bronze" as per case to be analyzed.
• After selecting material, import geometry as "Skill_Lync_Spur_Gear.stp".
• Go to the Model.
• Create Mesh for 0.5 mm element size as shown.
• Select geometry of both gears and rename it as "Left" and "Right"
• Give material assignment to both gears as per case.
• From the project tree, select "Connections" and create "Contacts".
Contacts :
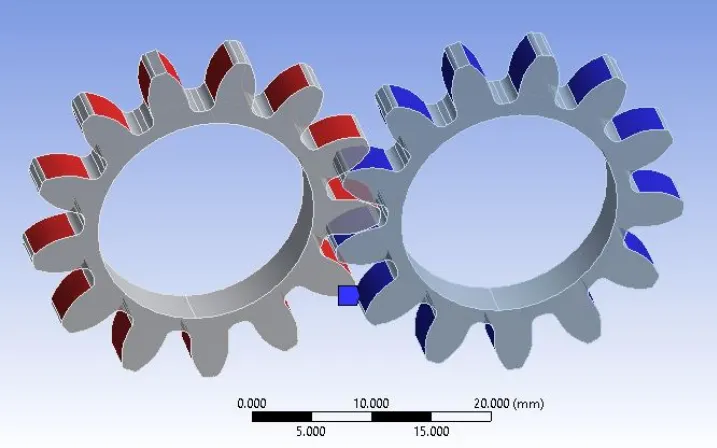
• For defining contacts between two gears, select faces of left gear as "Contact" and faces of right gear as "Target" for connection.
• There are 26 faces of each gear, must be selected.
• Select Contact type = Frictional. Because due to friction, there will be movement between gears.
• Select Behavior = Symmetric
• Select Formulation = Augmented Lagrange. As soon as teeth come in contact, it will tend to move from its position. So, Augmented Lagrange formulation reduces vibration an penetration and increases stiffness of gears.
• Select Interface Treatment = Adjust to Touch. Because if there is a gap between them or initial penetration, than this setting will help to adjust it and any error can be avoided.
Joints:
• After creation of connection between gears, create joints.
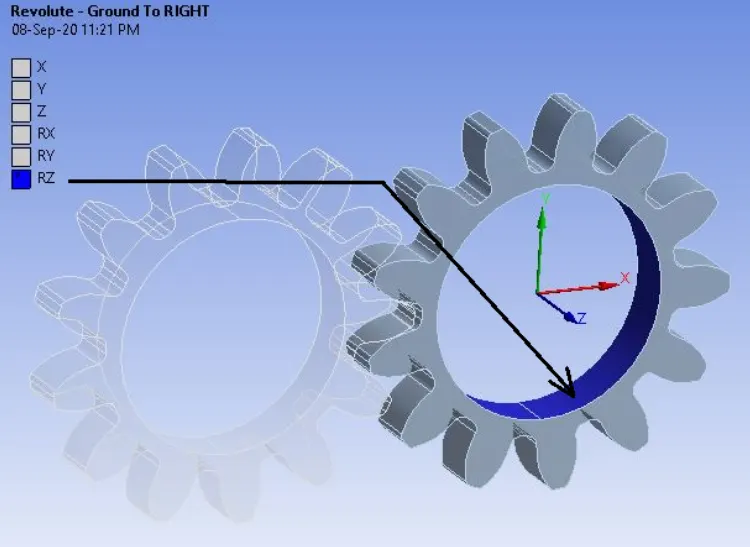
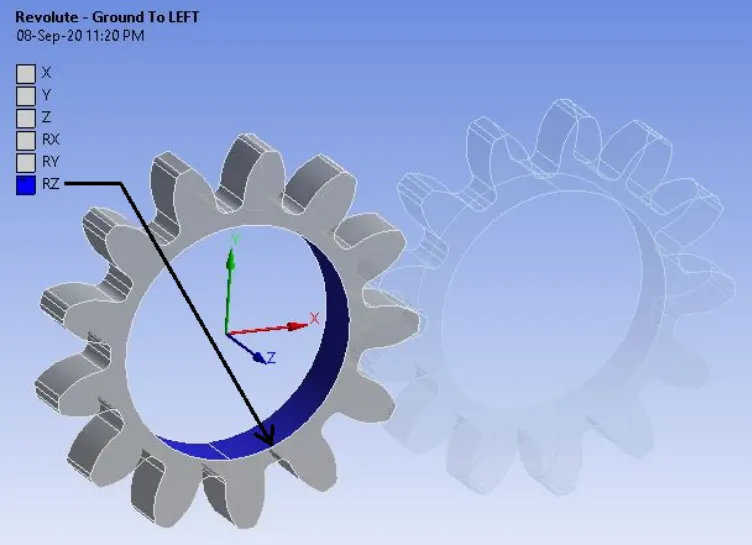
• Select inner face of each gear and give it a Revolute Joint as described in above image.
• For frame of reference for gears, select Connection Type = Body to Ground for both of the gears.
• We can see that in revolute joint, degree of freedom for gears automatically set to its axis or in RZ direction.
Boundary Conditions:
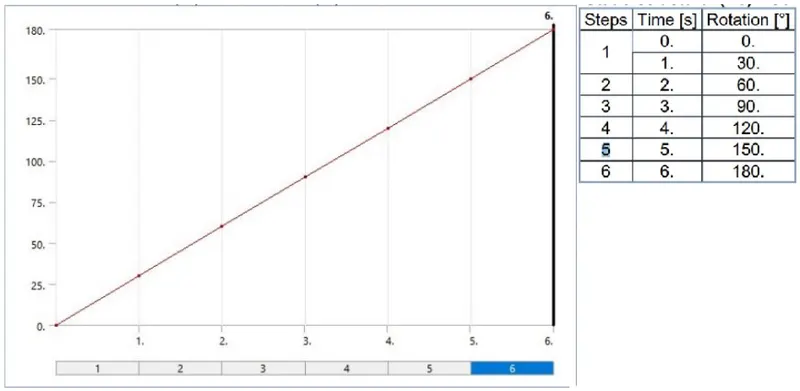
• Here we are going to look at contact forces, traces and stress developed for 1 revolution of gear. So for 180 degree angle, In analysis settings give values as given below:
No. of Steps =6
Auto Time stepping = ON
Defined by = Time
Initial Time Step = 0.2 s
Minimum Time Step = 0.05 s
Maximum Time Step = 0.5 s
Select all 6 steps and select "Large Deflection = ON" in solver controls.
• Other Boundary conditions for joints are as given below:
• Joint Load:
Joint: Revolute - Ground to Left
Type: Rotation
Magnitude: Tabular Data
Tabular Data:
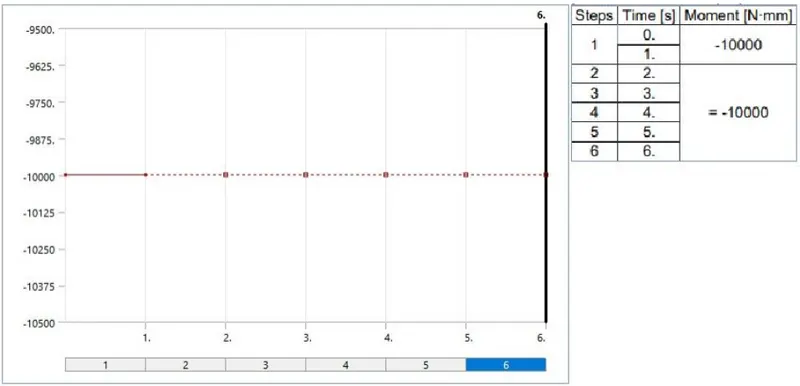
• Joint Load:
Joint: Revolute - Ground to Right
Type: Moment
Magnitude: Tabular Data
Tabular Data:
Solution:
• After giving proper boundary conditions, create desired solutions for output results.
• Create Solutions for "Equivalent (Von Mises) Stress, "Total Deformation" and for "Stress Intensity"
• Also give Contact Tool and create solutions for contact "Status" and "Pressure".
Results :-
Results for all cases are given below :
CASE_1 :- (Material = Cast_Iron(Ductile))
Material Specification :
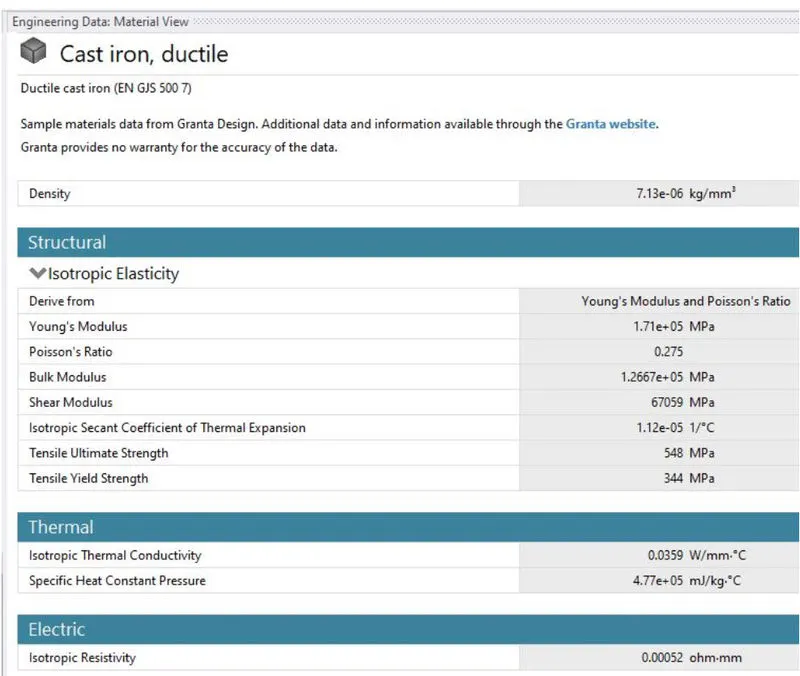
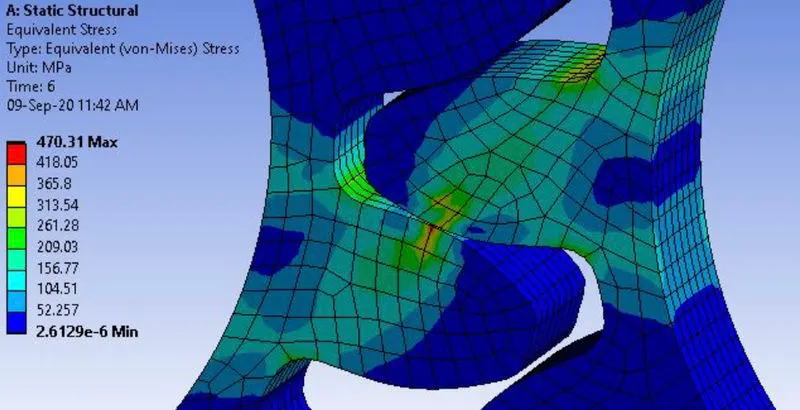
Stress Contours :
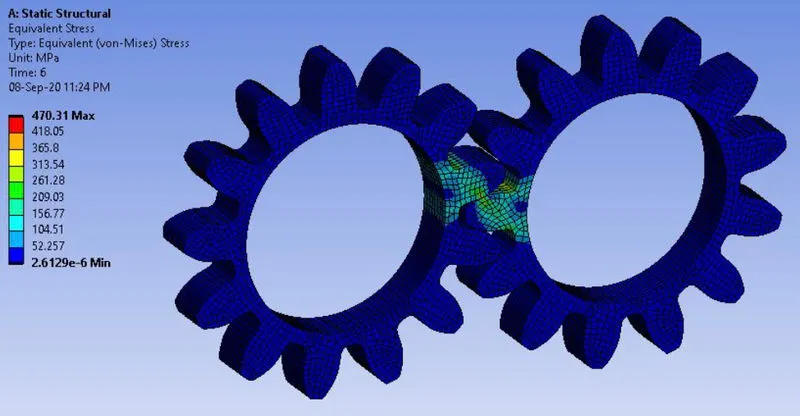
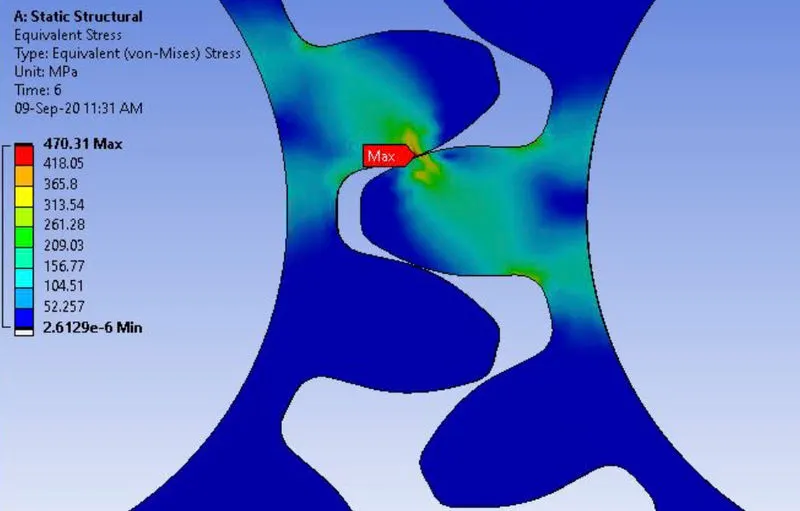
Stress Plot :
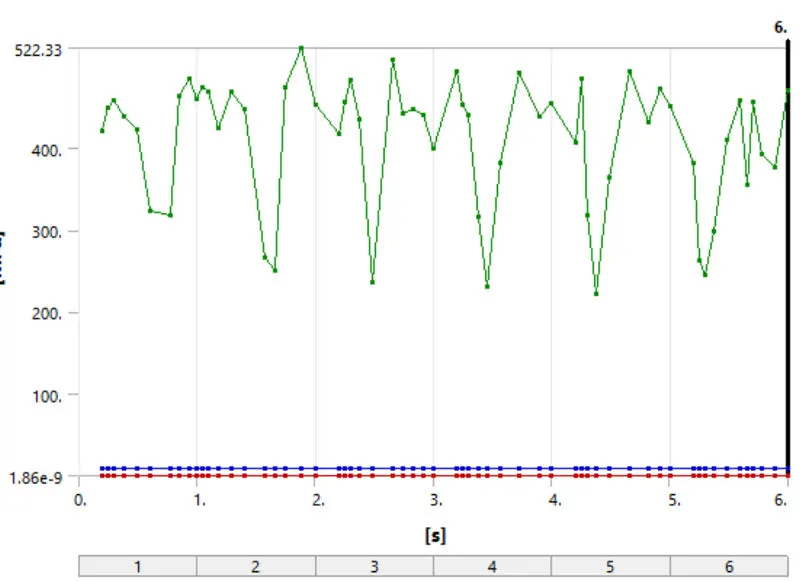
Detailed Stress Values :
• Stress data given below has been short listed for convenience .
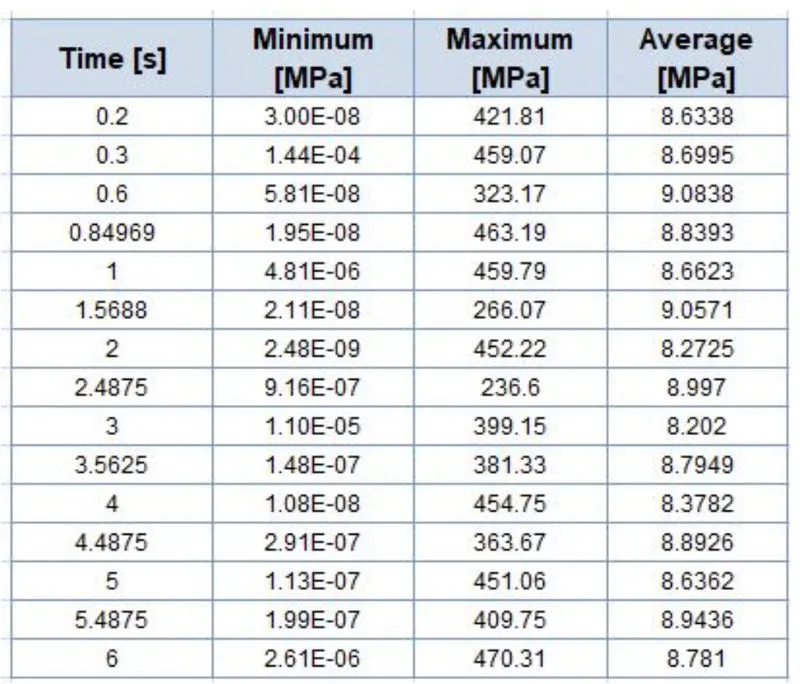
• Here we can see that maximum stress induced in gears is 470.31 MPa.
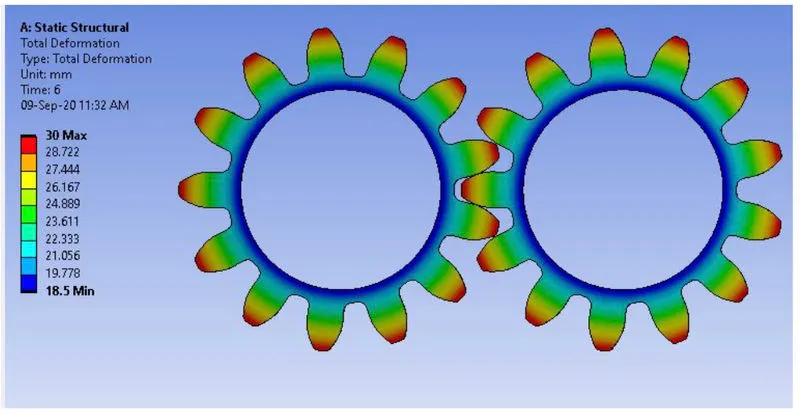
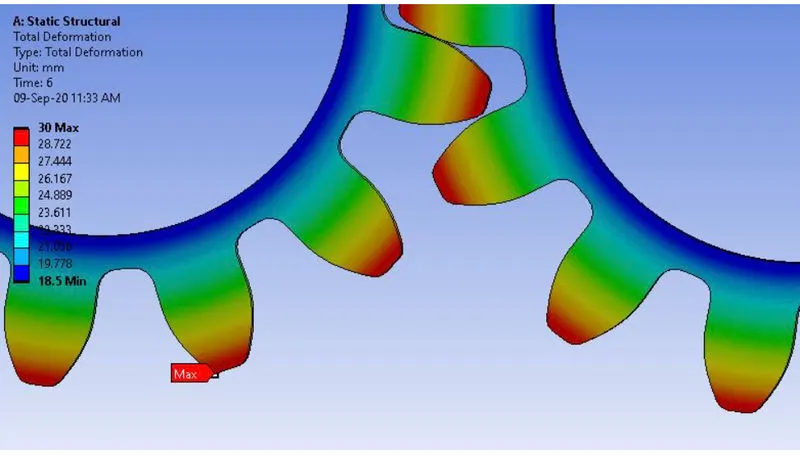
Deformation Contours :
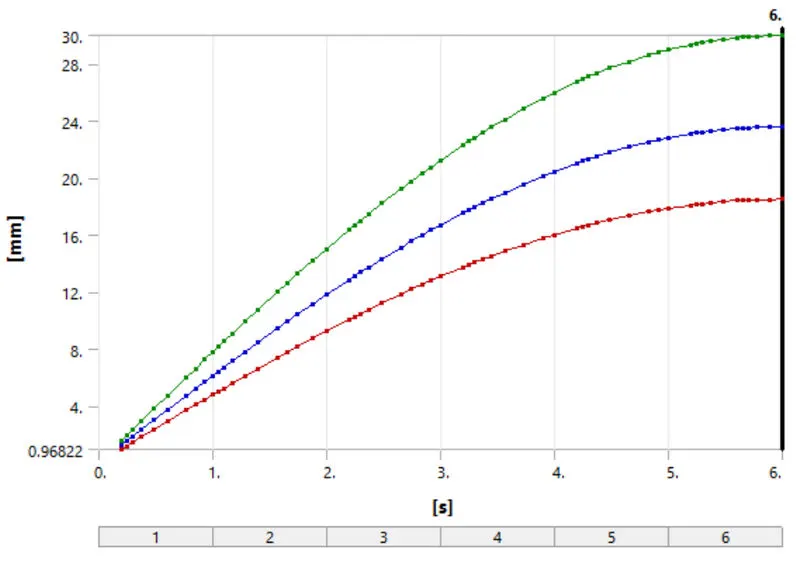
Deformation Plot :
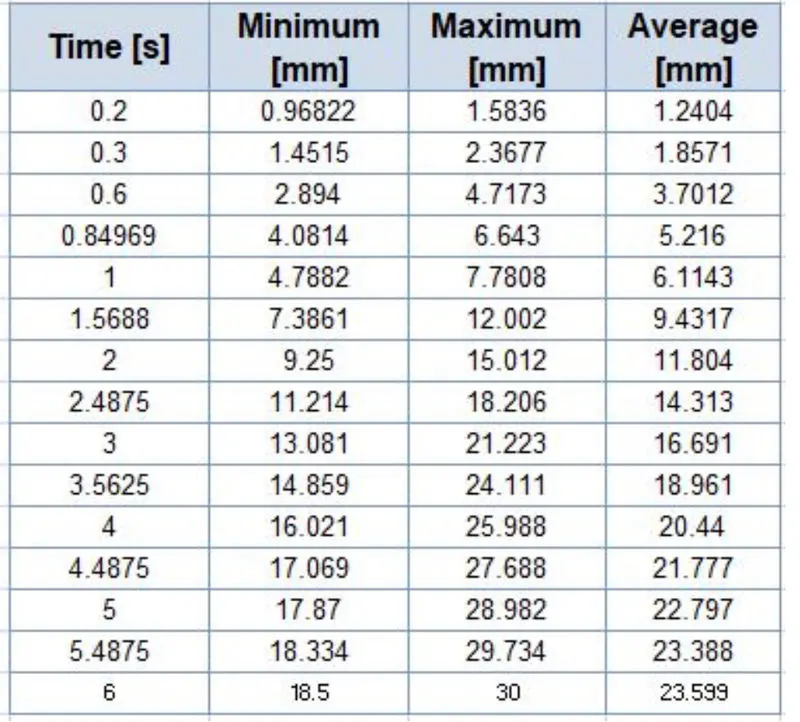
Detailed Deformation Values :
Stress Intensity Contours :
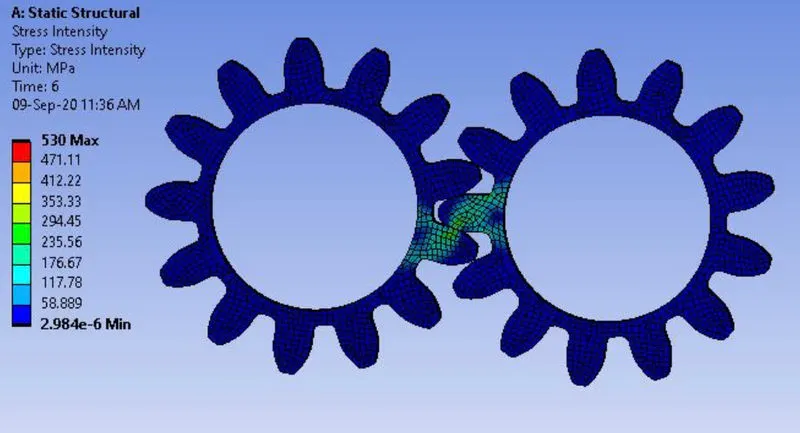
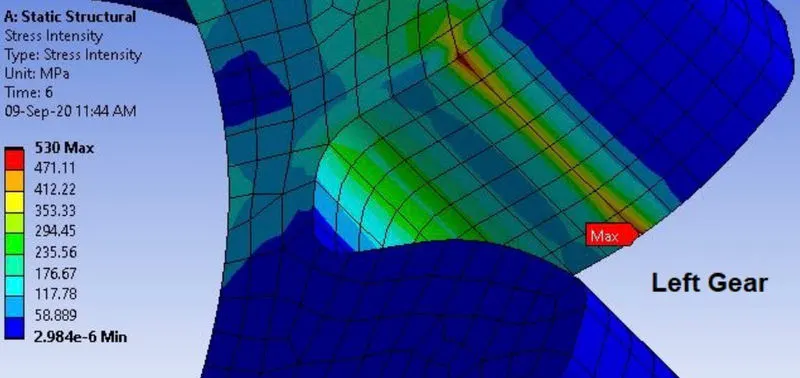
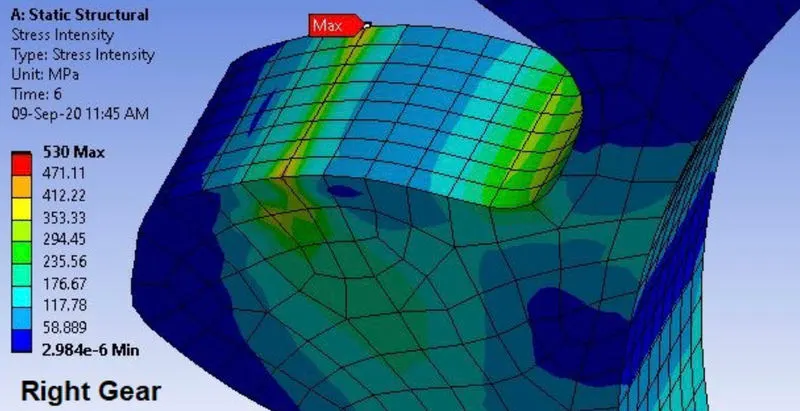
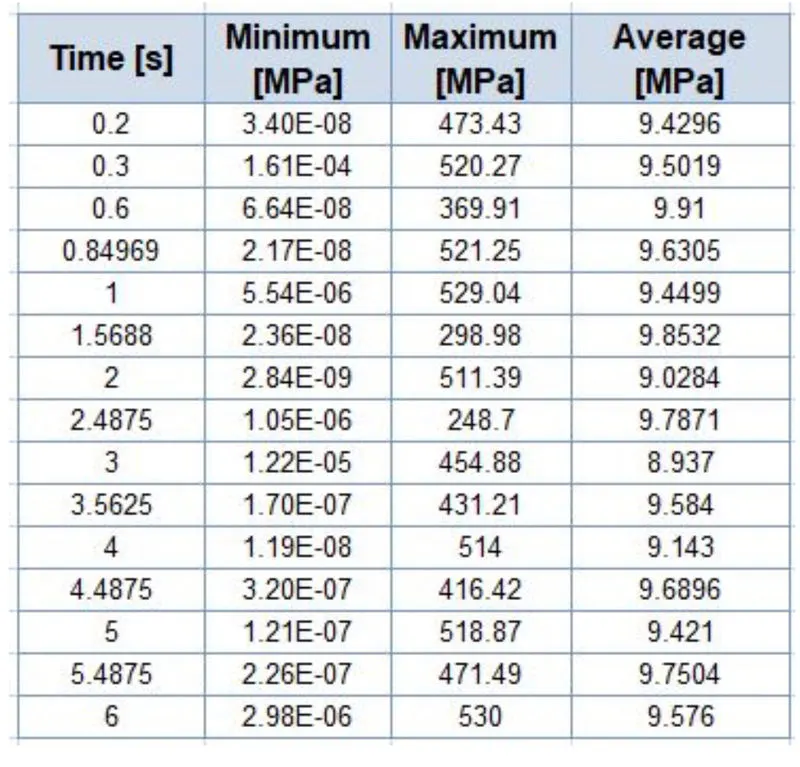
• Maximum Stress Intensity is 530 Mpa. Beyond this value, we can assume that crack propogation will start from the edge shown in above image of left and right gear.
Stress Intensity plot :
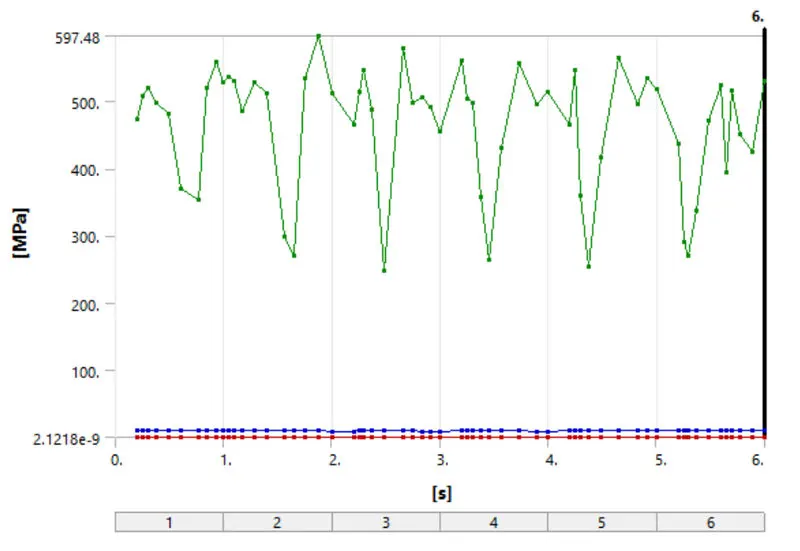
Detailed Stress Intensity Values :
Contact Status :
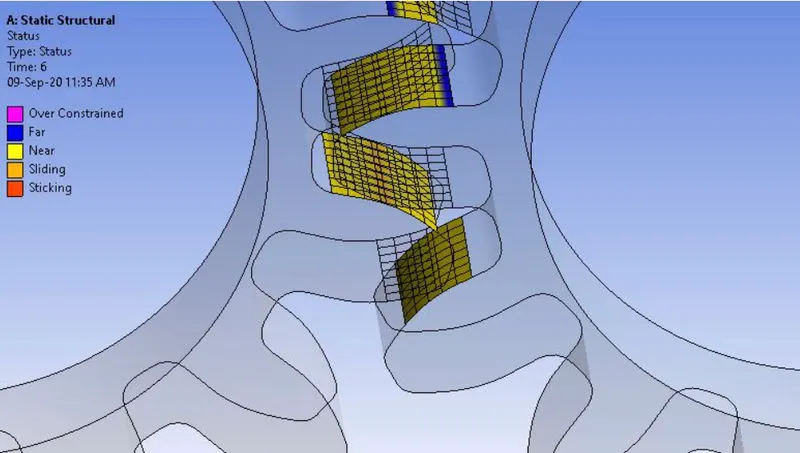
• Here we can see the orange portion, which denotes sliding at contact portion of gears.
• Also we can see near and far areas of contact in yellow and blue colors.
• Sticking is not observed here.
• Also there is no over constrained area in gear contacts.
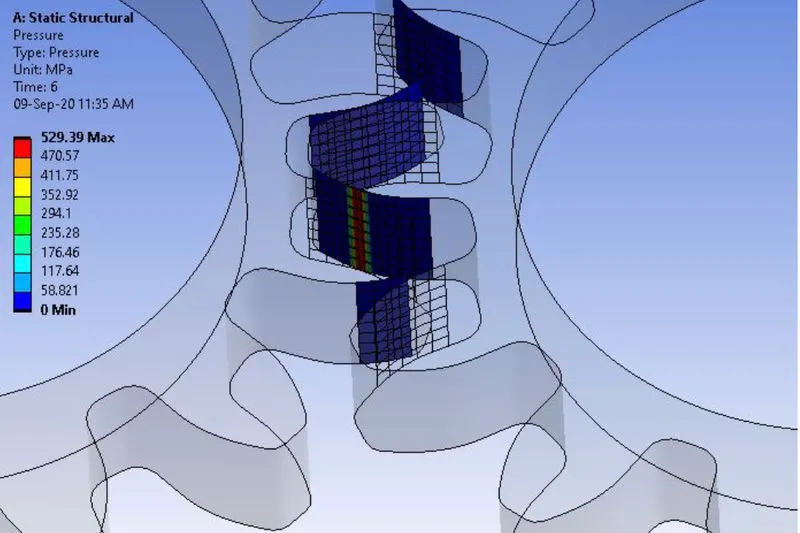
Contact Pressure :
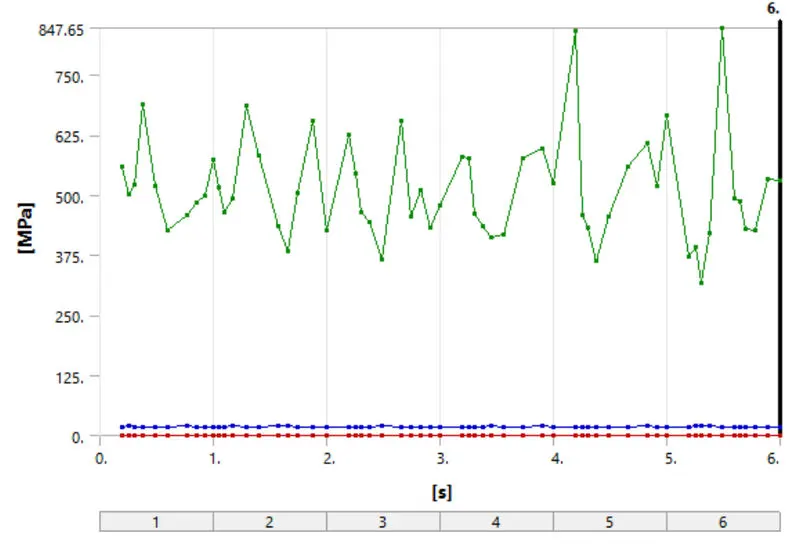
Pressure Plot :
Detailed Pressure Values :
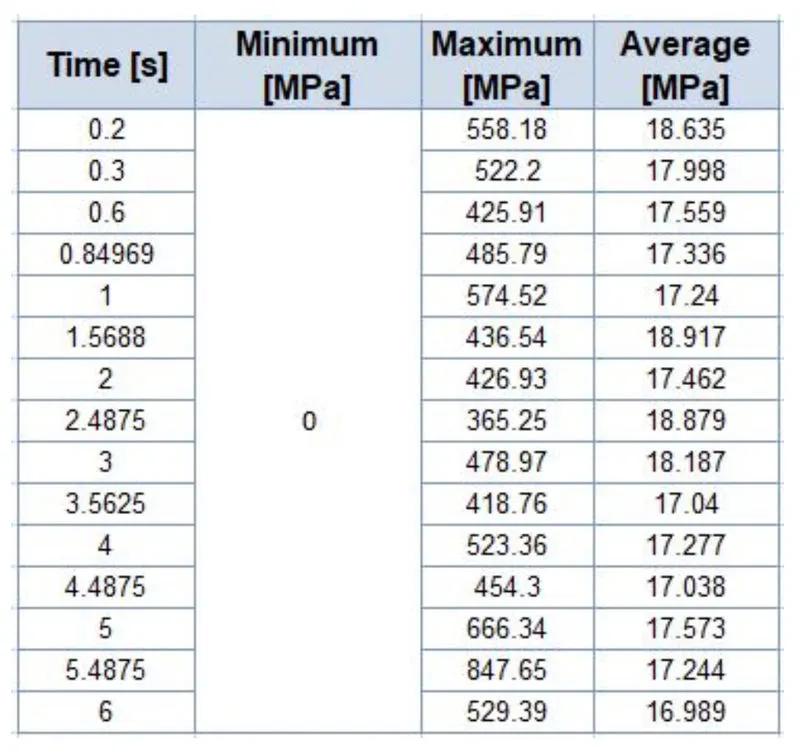
• Here we can see the highest pressure generation at contacts faces.
• Also from tabular data, maximum pressure generation is 847.65 Mpa at 5.48 s.
---------------------------------------------------------------------------------------------------------------------------------------------
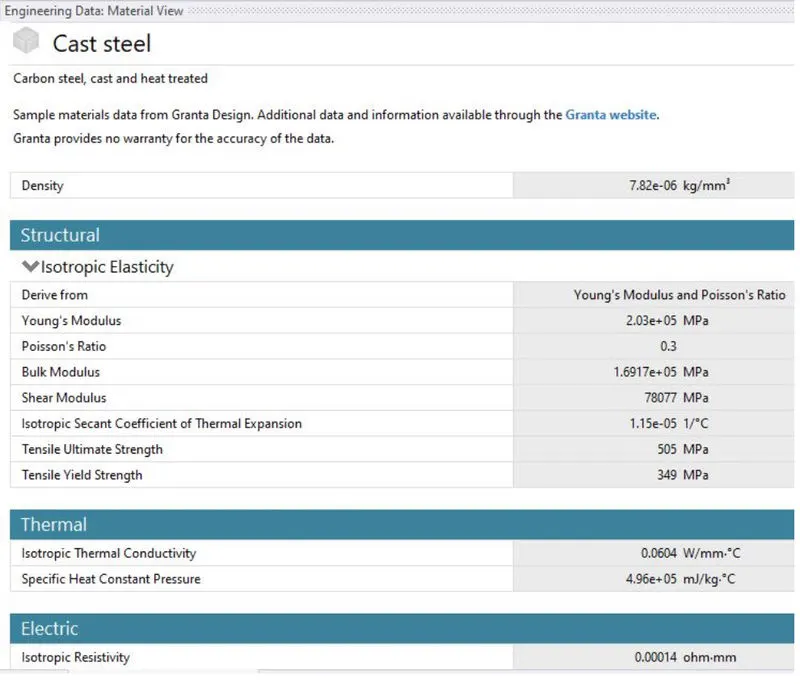
CASE_2 :- (Material = Cast_Steel)
Material Specification :
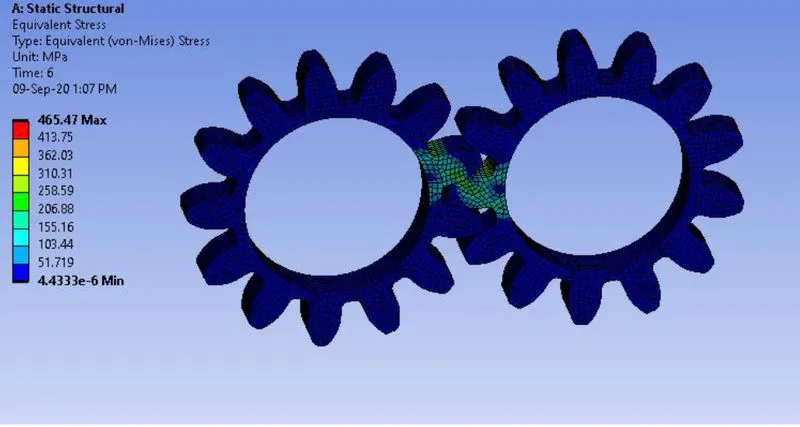
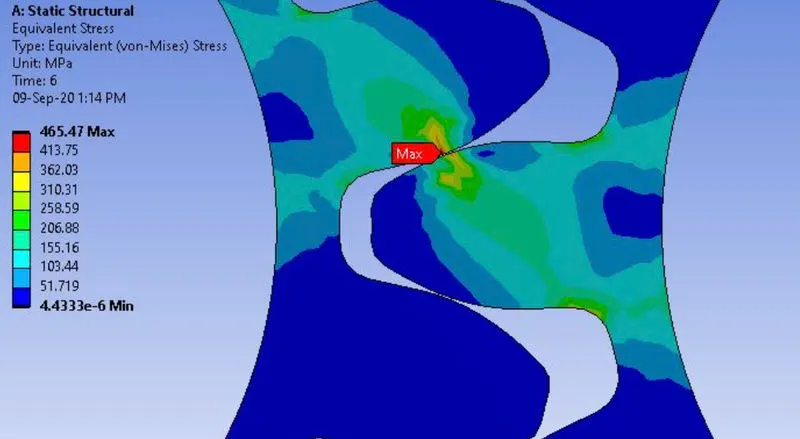
Stress Contours :
Stress Plot :
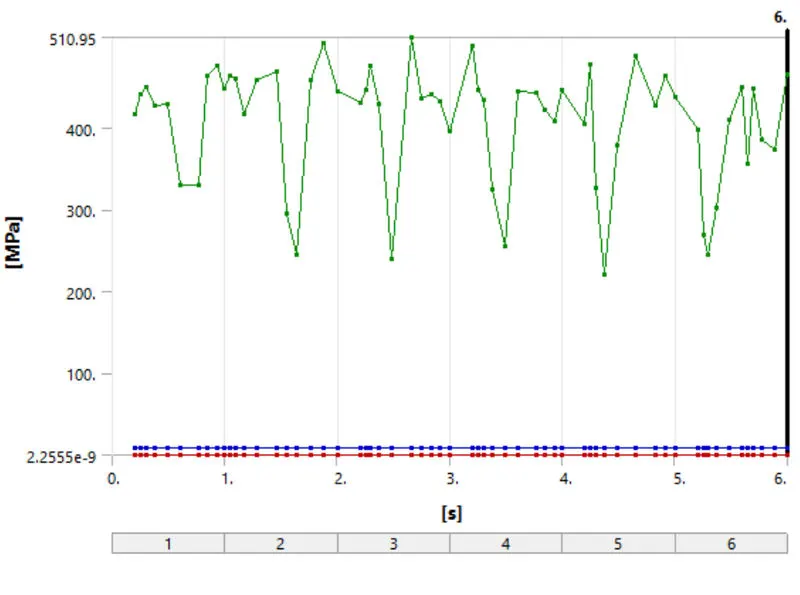
Detailed Stress Values :
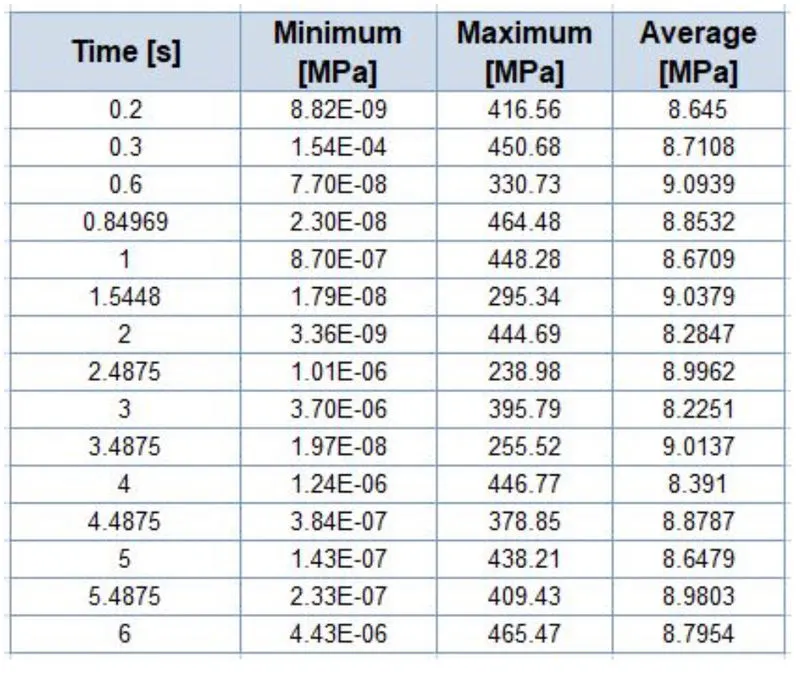
• Stress data given below has been short listed for convenience .
• Here we can see that maximum stress induced in gears is 470.31 MPa.
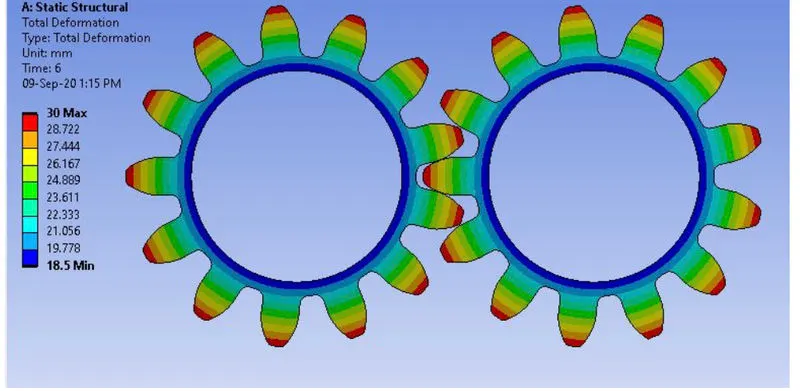
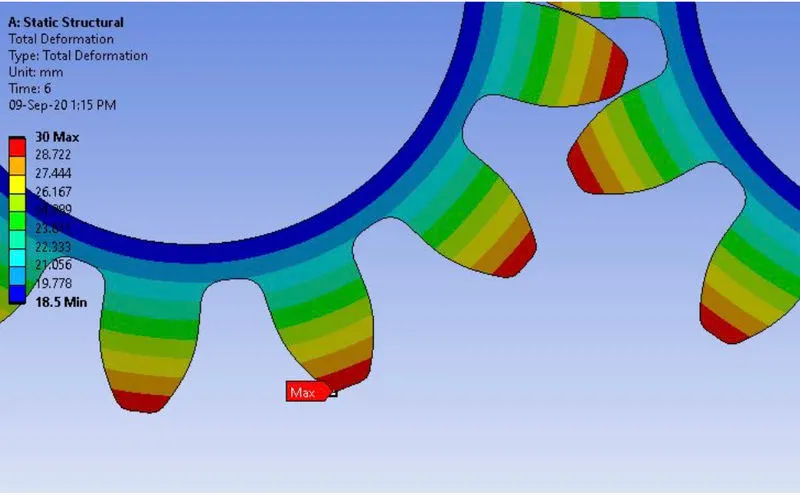
Deformation Contours :
Deformation Plot :
Detailed Deformation Values :
Stress Intensity Contours :
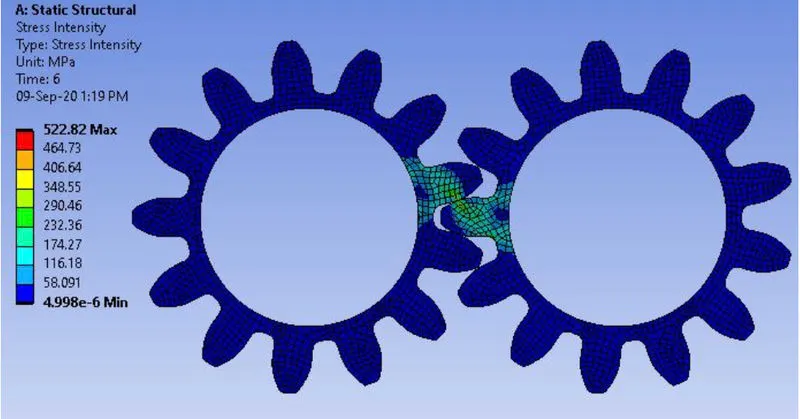
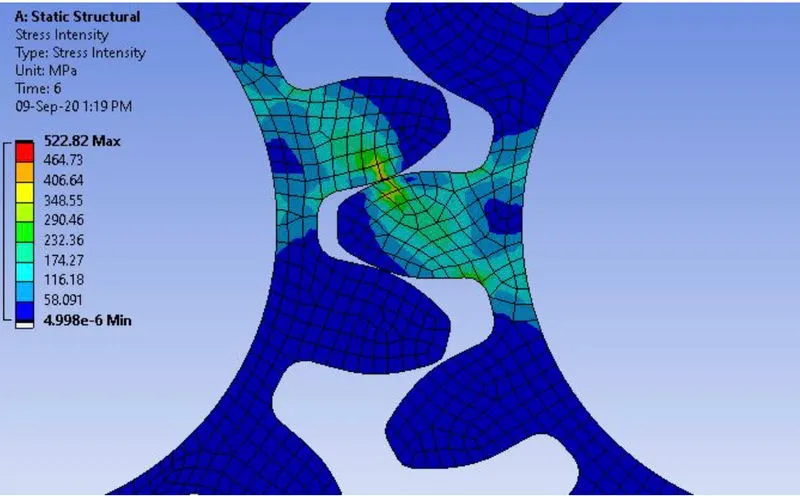
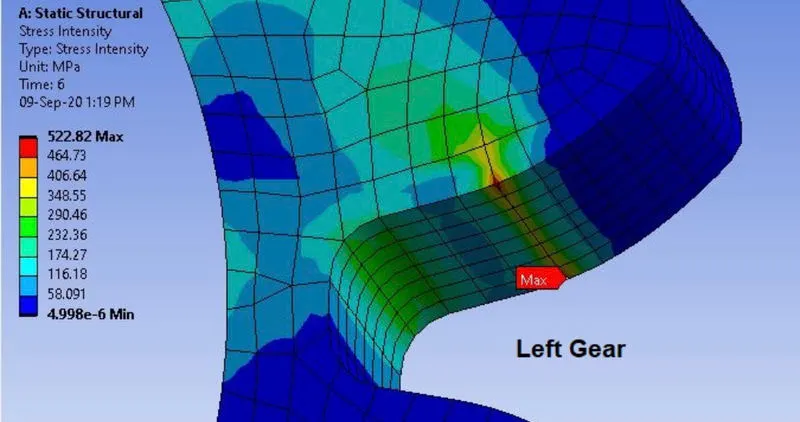
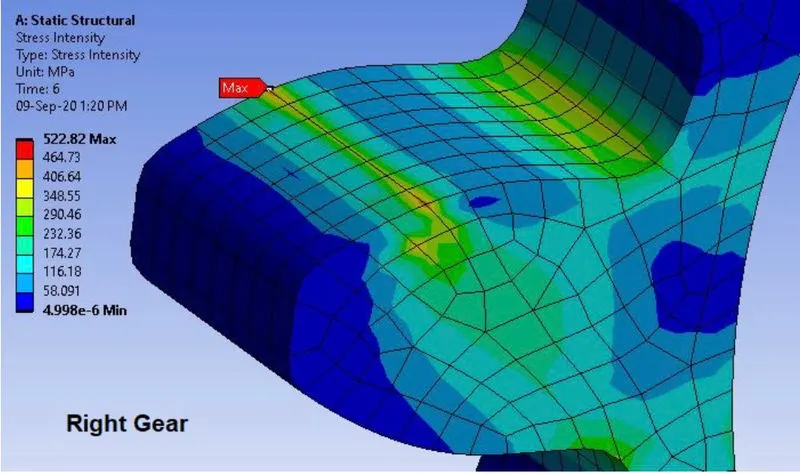
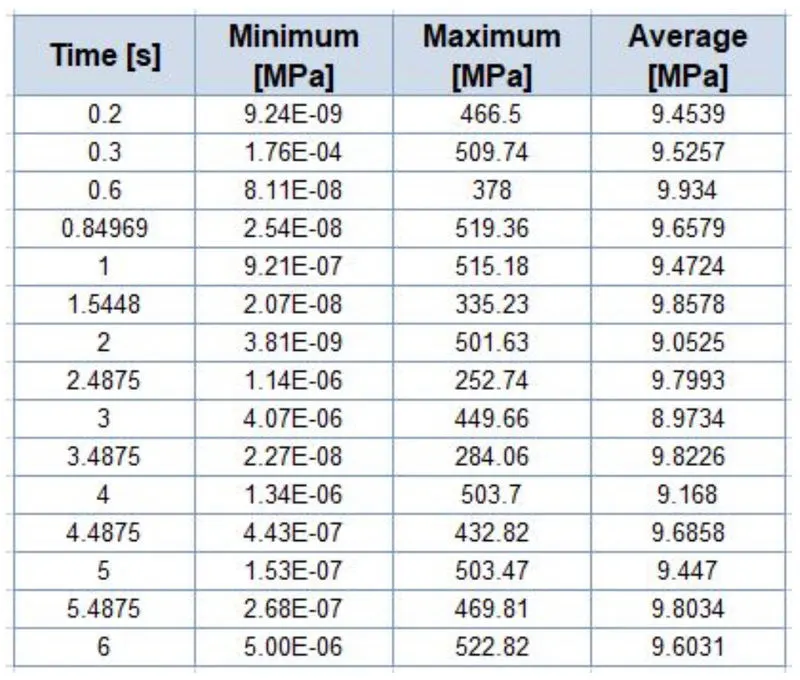
• Maximum Stress Intensity is 522.82 Mpa. Beyond this value, we can assume that crack propogation will start from the edge shown in above image of left and right gear.
Stress Intensity plot :
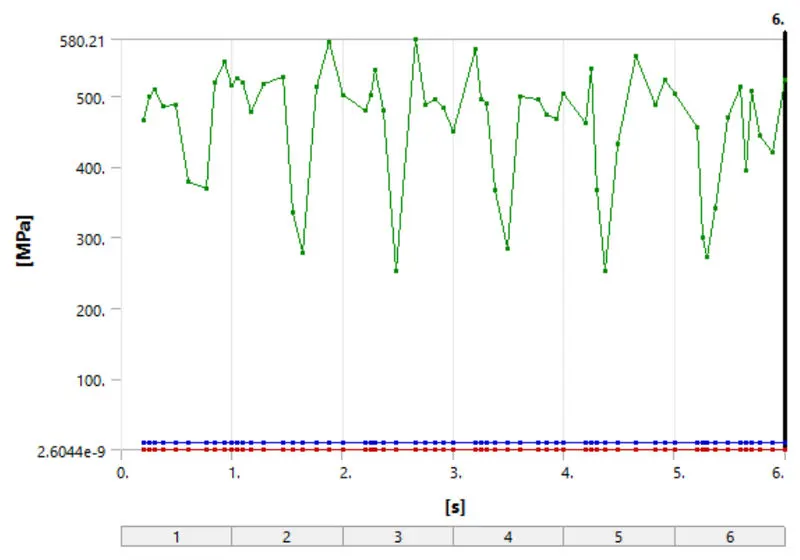
Detailed Stress Intensity Values :
Contact Status :
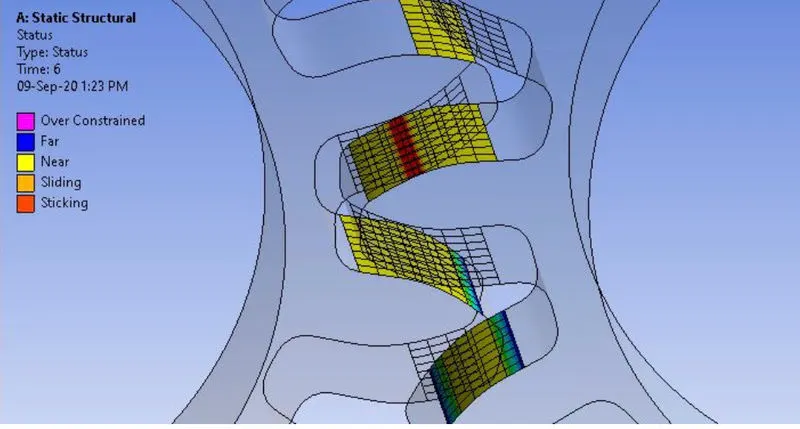
• Here we can see the Sliding as well as sticking at the contact faces.
Contact Pressure :
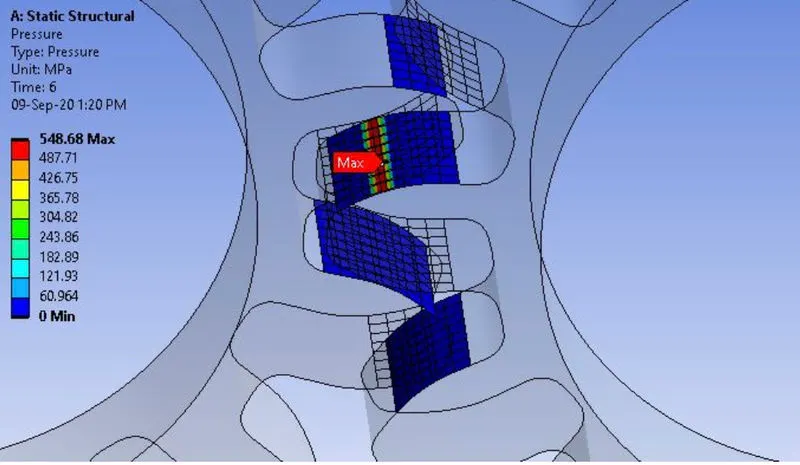
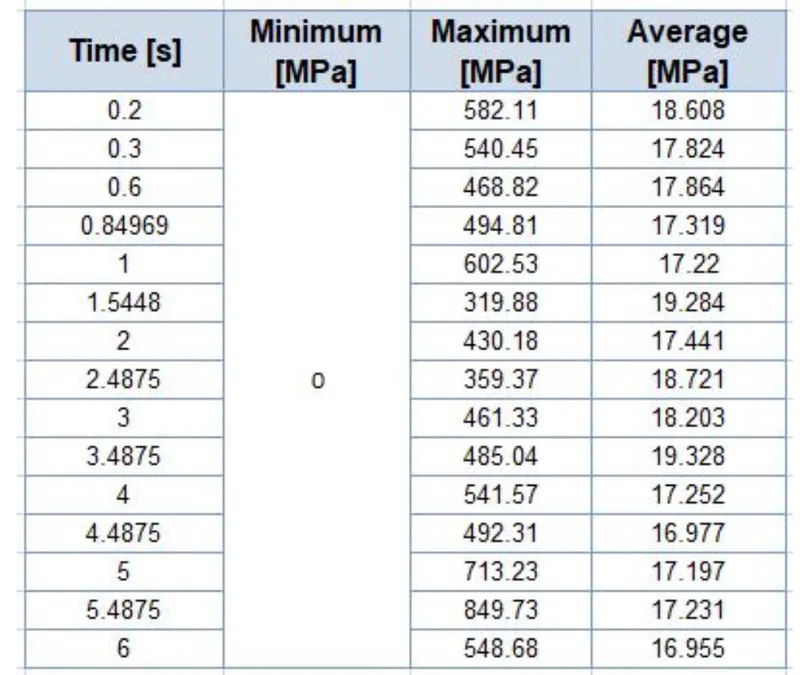
• Also from tabular data, maximum pressure generation is 849.73 Mpa at 5.48 s.
Pressure Plot :
Detailed Pressure Values :
---------------------------------------------------------------------------------------------------------------------------------------------
CASE_3 :- (Material = Cast_Bronze)
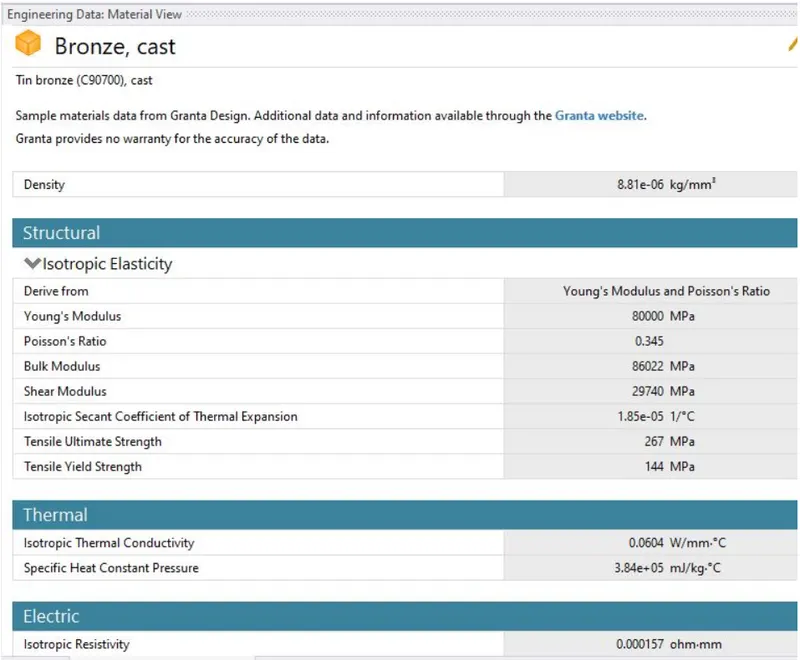
Material Specification :
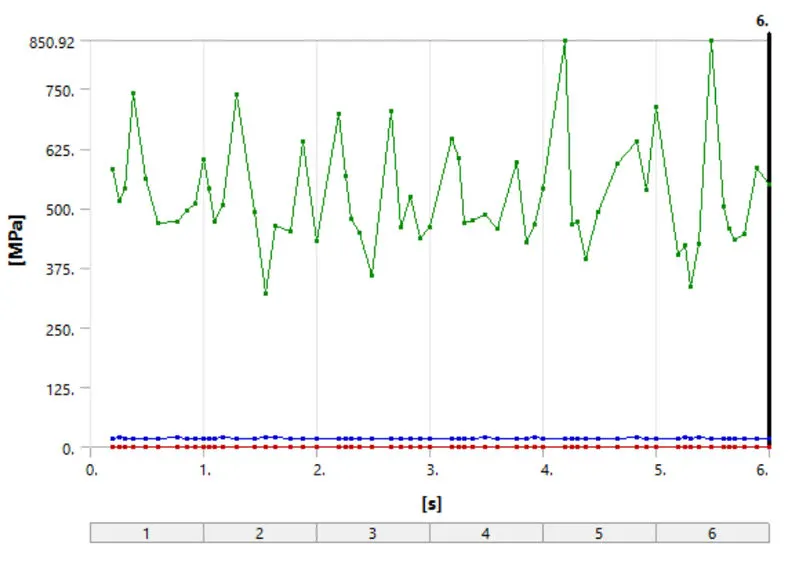
Stress Contours :
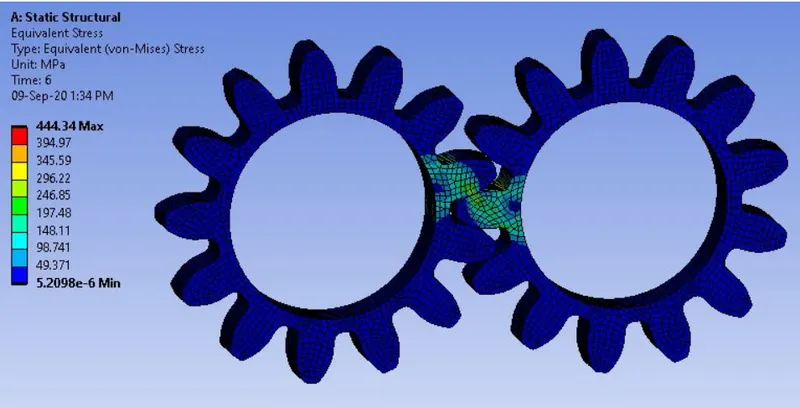
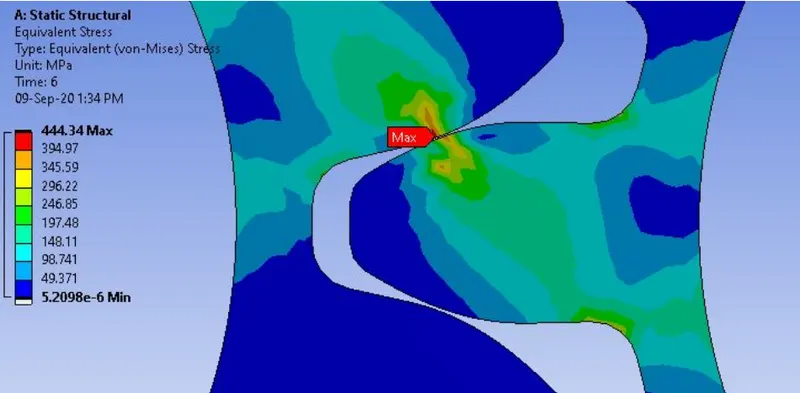
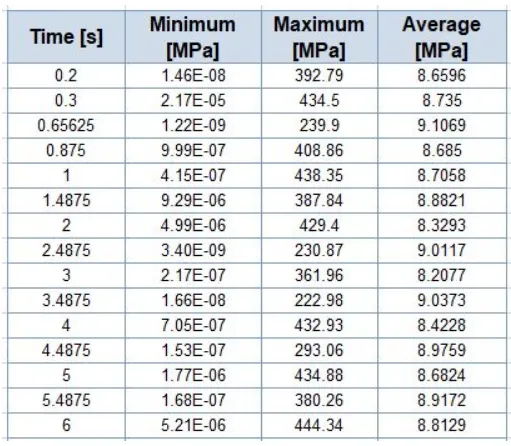
• Here we can see that maximum stress induced in gears is 444.34 MPa.
Stress Plot :
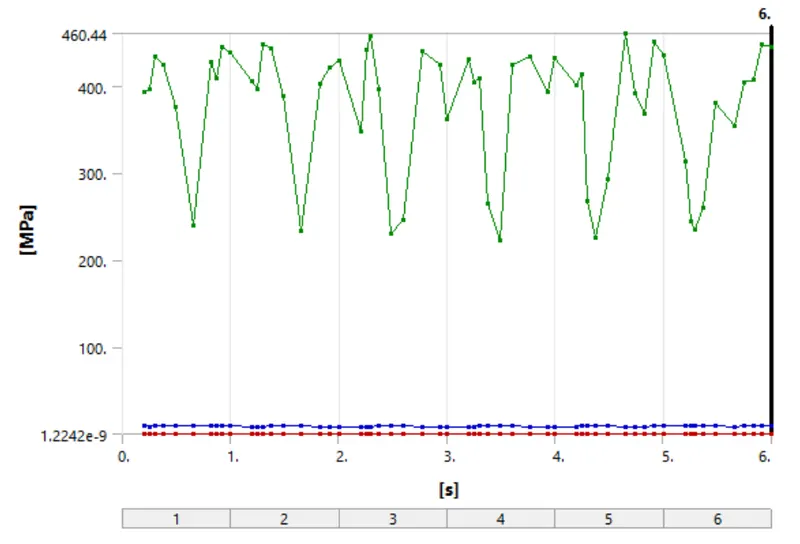
Detailed Stress Values :
Deformation Contours :
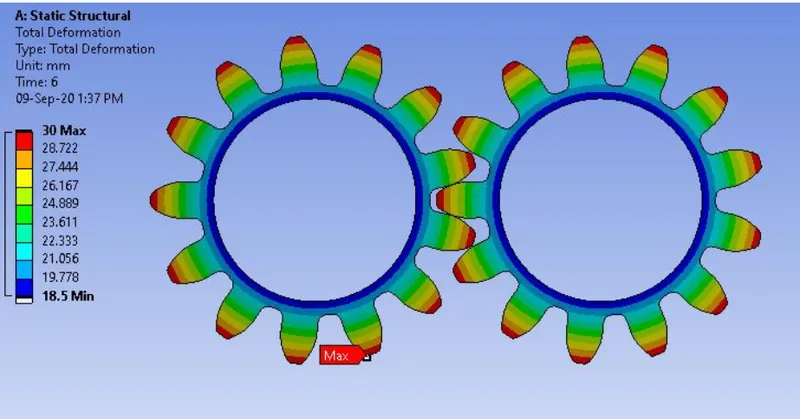
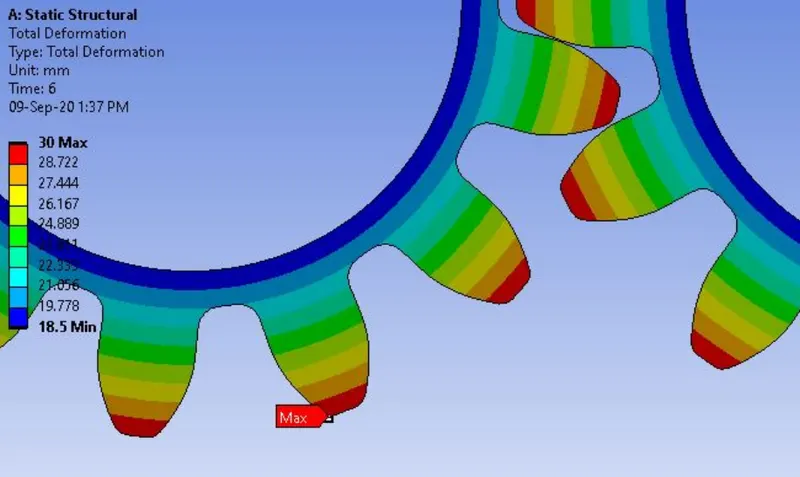
Deformation Plot :
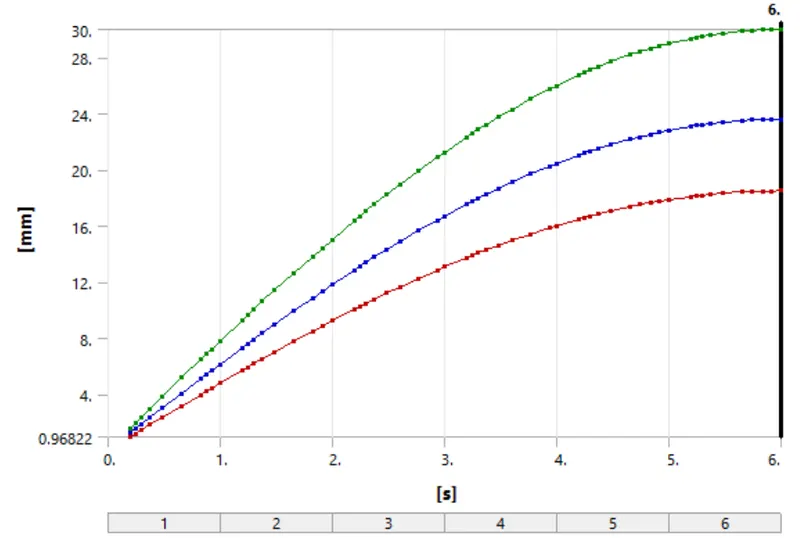
Detailed Deformation Values :
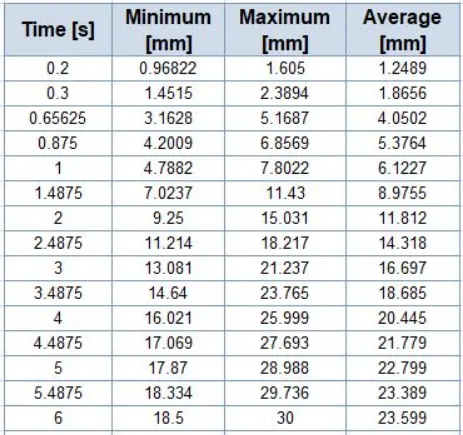
Stress Intensity Contours :
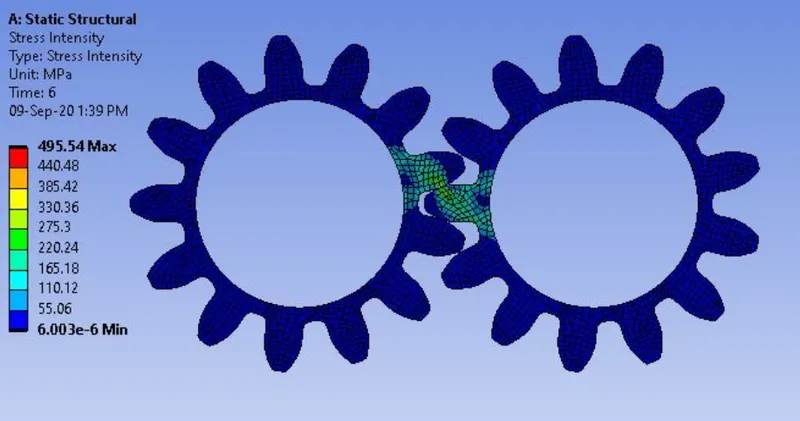
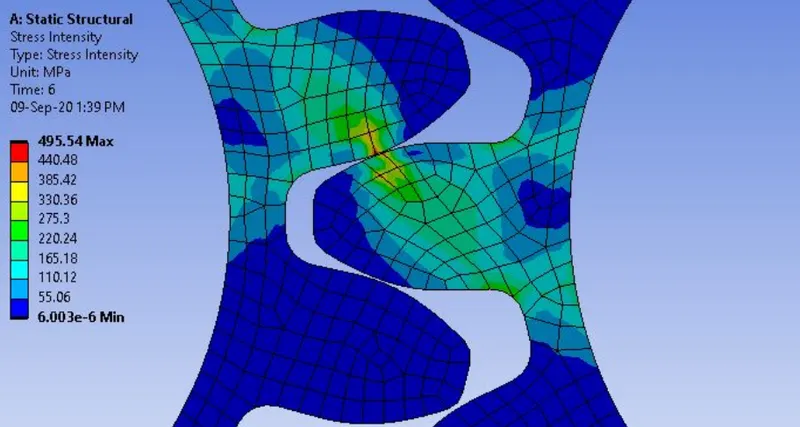
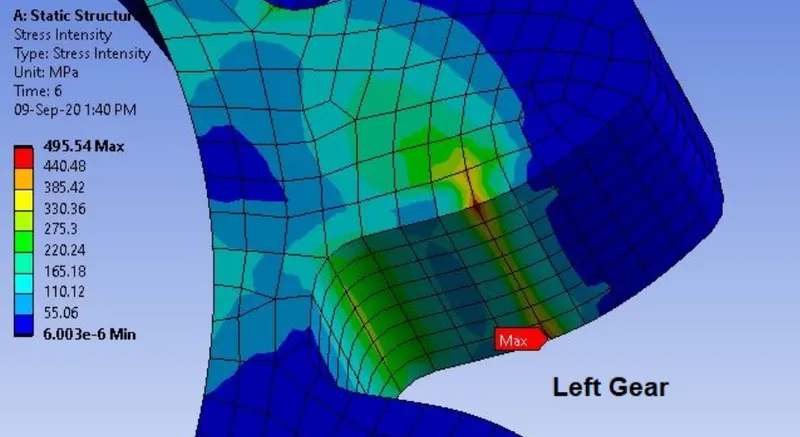
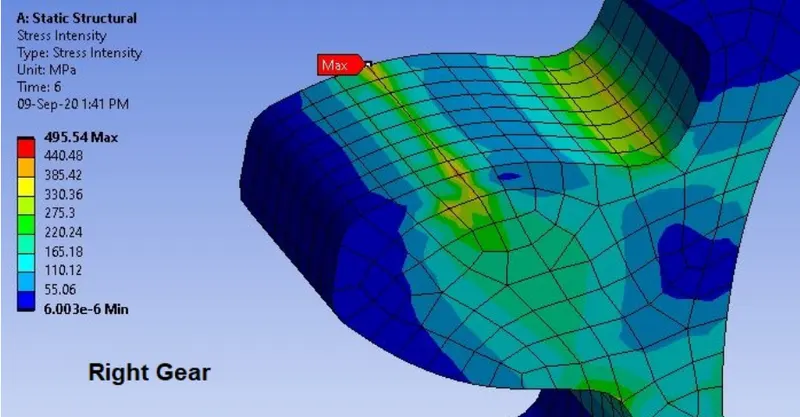
• Maximum Stress Intensity is 495.54 Mpa. Beyond this value, we can assume that crack propogation will start from the edge shown in above image of left and right gear.
Stress Intensity plot :
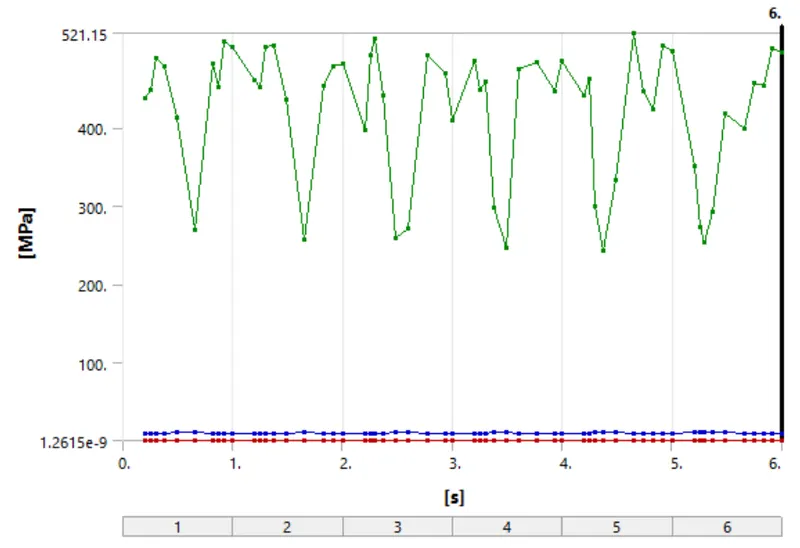
Detailed Stress Intensity Values :
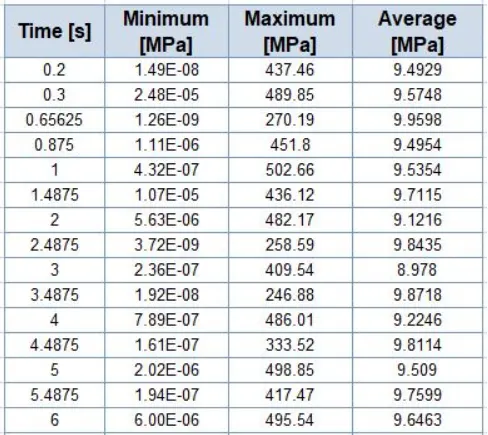
Contact Status :
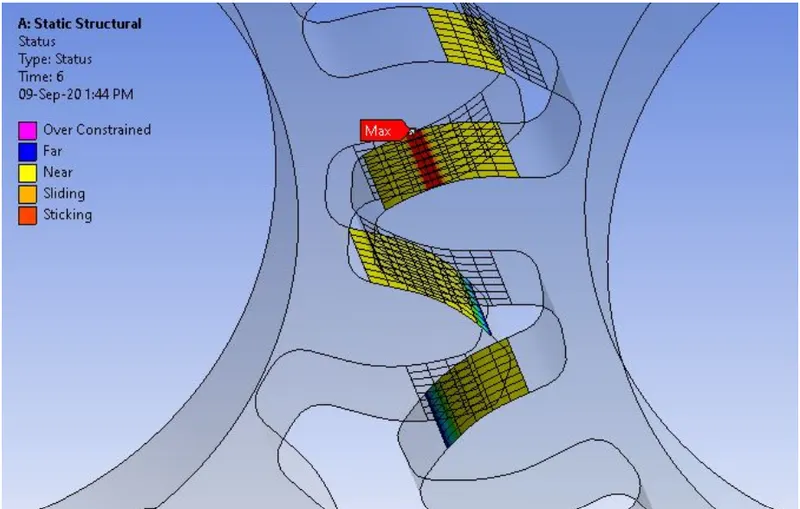
• Here we can see the Sliding as well as sticking at the contact faces.
Contact Pressure :
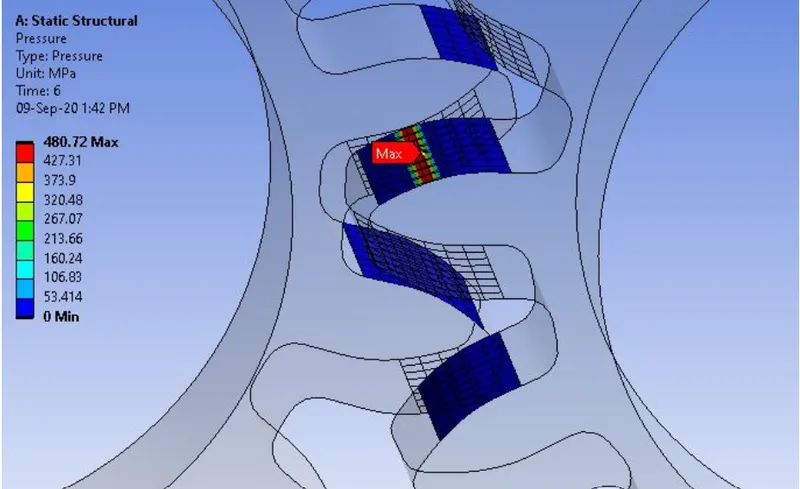
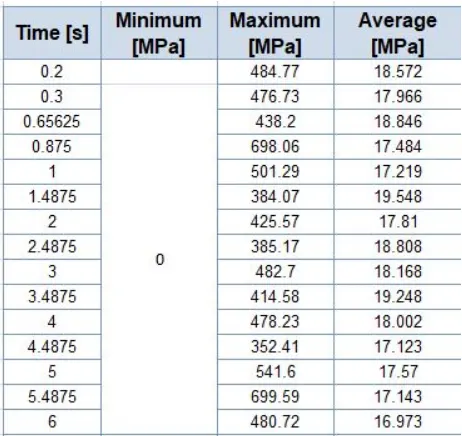
• Also from tabular data, maximum pressure generation is 699.59 Mpa at 5.48 s.
Pressure Plot :
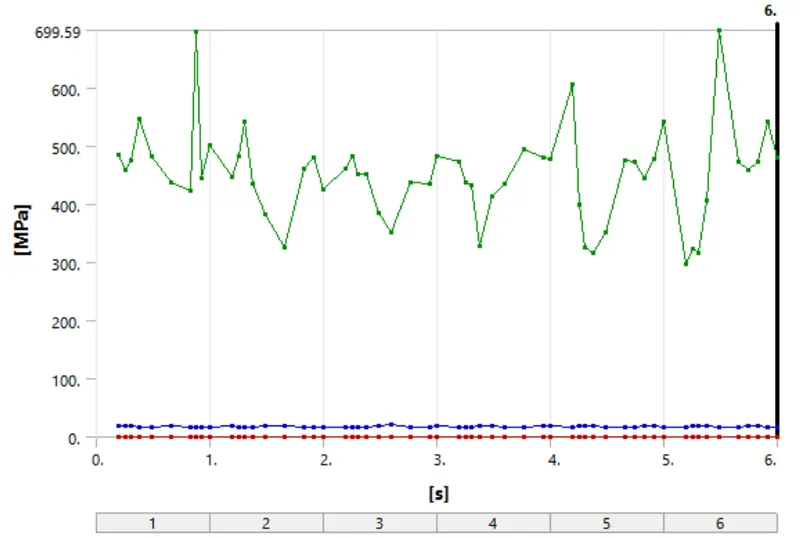
Detailed Pressure Values :
---------------------------------------------------------------------------------------------------------------------------------------------
Comparison :-
| CASE | Max.Equivalent(Von Mises) Stress(Mpa) | Max. Stress Intensity(Mpa) | Max. Total Deformation(mm) |
| Case_1 | 470.31 | 530 | 30 |
| Case_2 | 465.47 | 522.82 | 30 |
| Case_3 | 444.34 | 495.54 | 30 |
• We can compare that relation in Equivalent Stress for all case is CASE_1> CASE_2›CASE _3.
• Also for Stress intensity it is CASE_1 > CASE 2>CASE 3.
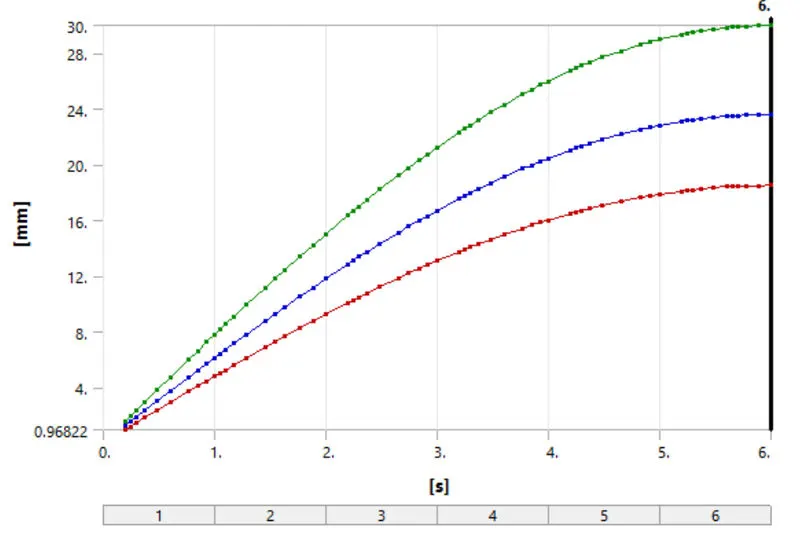
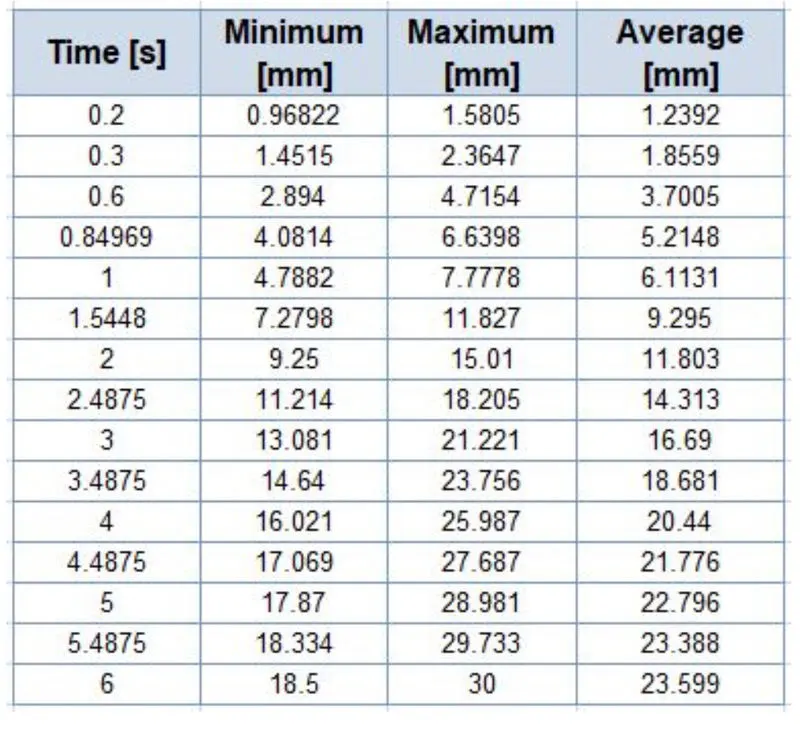
• Deformations in all cases are same.
---------------------------------------------------------------------------------------------------------------------------------------------
Conclusion :-
• As per above results, we can see that Cast _Iron (Ductile) material has highest stress and stress intensity. Generally Cast Iron gears are easy to manufacture, and durable, but it also wear and tear very fast. So we should avoid Cast iron as a material for gears.
• There are variety of carbon steel used for gears, due to their convenient process of heat treatment like case hardening, thru hardening and machinability. So Cast Steel is good material compared to Case Iron.
• Cast Bronze is generally used for Spur and Worm gears. Copper alloy (bronze) gears have unique properties that contribute to minimal wear in bronze to steel contact. Bronze gears are used in gear reducers and are mated against steel worm gears. Bronze spur gears are used in other devices where they are required to mate with steel spur gears.
• So from the above analysis stand point we can choose Cast Bronze as a material for gears.