Week 1:- Introduction to BiW and Fixtures Challenge
- What is BIW & define its parts?
- Body in white (BIW) refers to the welded sheet metal component which for the vehicle structure to which the other components will be married, i.e. engine, chassis, exterior & interior trim.
- BIW refers to the stage in the automobile manufacturing in which a car body’s components have been joined together; using one or a combination of different techniques: welding, riveting, clinching, bonding, laser brazing etc. BIW is termed before painting and before the motor, chassis sub-assemblies, or trim have been assembled in the frame structure.
- BIW parts are mainly categorized as below
- Underbody structure
- Frond end structure
- Body side structure
- Closure
- Roof
- All those substructures consist of the following major panels: -
- Underbody structure: -
- Dash panel provides partition between engine and the driver cabin.
- FRT floor provides base for seats
- Raiser connects front floor to rear floor by providing level difference.
- Rear floor: - floor on the rear of the car and provides partition from ground and base for rear seats
- Rear wheel house
- Front End Structure: -
- Plenum panel a chamber located between the throttle body and runners of the intake manifold.
- FRT wheel house is an encasement around the front wheel
- Wing panel outer most side panel in the front.
- Cowl: - portion of the body bounded by the front fenders, the base of the win shield and the rear edge of the hood.
- Upper tie bar: - upper panel in front connecting the two sides of front structure.
- Lower tie bar: - lower panel in front connecting the two sides of front structure.
- Body Side Structure: -
- A-pillar: - front most support to the roof
- B-pillar: - second support to the end
- C/D-pillar: - c is a rear most support to roof in case of two row seating system, it will be third one. D is the fourth support usually rear side of the quarter panel.
- Ring panel: - a structure panel connecting the rear and front portion.
- Quarter panel: - rear most panel of a body side structure.
- Drip rails / Gutters: - an exposed channel applied to the roof over the side windows to direct water away from the windows.
- Closures: -
- All doors
- Hoods / Bonnet – a hinged panel providing access to the engine compartment.
- Roof structure: -
- Roof
- Headers – structural member above the win shield at juncture with the forward edge of the roof panel.
- Bows
- What do you understand by BIW nomenclature?
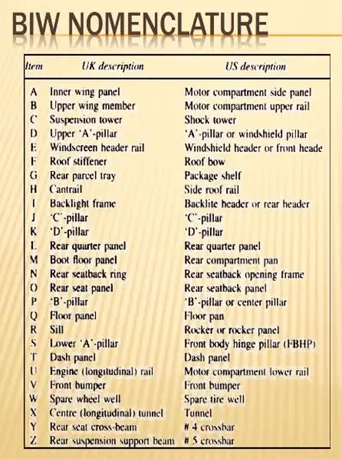
- Nomenclature is basically choosing name for things. BIW have many parts in it. All parts have its different names. As automotive industry is separate worldwide. Every nation has its own language. So, the same part in BIW have different name in its region. One component is called inner wing panel in U.K. and same component called motor compartment side panel in U.S.
- Below figure shows the UK & US nomenclature: -
- What is fixture and its type?
- Fixture is device which holds the work piece to be processed by using 3-2-1 principle.
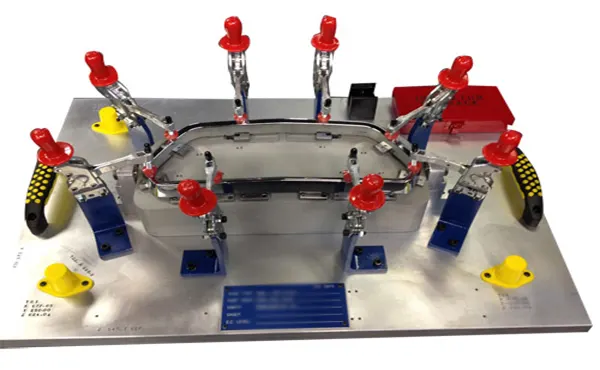
- In general, a welding fixture consist of number of units together to hold the car panel, and is mounted on a base unit.
- Types of fixtures
- Production fixture: - As a name suggest this fixture is used for mass production. It is fixture on which a car body get assembled and go to end customer. These types of fixture require high consistency through its operation to maintain geometry of parts. So, material used for this type should be well tested as well as hardness level aesthetic. The quality in terms of dimension, tolerance should be met. These fixtures need to maintain after certain period of time. The assembly and disassembly should be easy as low as possible. So, maintenance person can easily access with saving time.
- Pre-production fixture: - it is generally defined as prototype fixture. It is designed to study feasibility of initial batch production to check which things are need to be improving before starting production. This fixture is base of production fixture in benchmark and criteria and help us to rectify error. In production operation fixture there will be more involvement of manual operations, engineer and quality person. It has larger cycle time than production fixture. But won’t practice by designing production fixture because it takes lots of time cost. We have to maintain cost of car as low as possible so we directly go production fixture by considering standards, checklist to maintain error free production.
- Checking fixtures: - As name suggest this fixture is used for checking assembly which came out from geo fixture. Checking fixture are same as geo fixture except there are no operation done like welding, gluing or hemming. Instead of that we use different in built gauges or external gauges to check various dimensions, gap, relative dimension, tolerance. These data are compared with data provided by designer or design team of that particular. The geometry of welded part also checked in this fixture to ensure part maintains the required dimensions and geometry.
- What is the basic principle of fixture design?
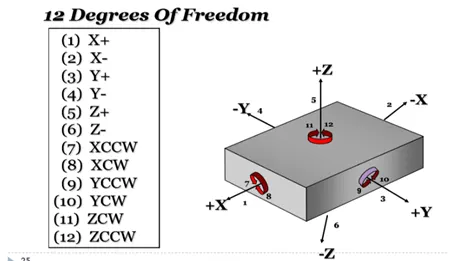
- For fixture designer, the major portion of design time is spent deciding how to locate a work piece in the fixture. You know that any free body has total 0f twelve degrees of freedom as below:
- 6 translational degrees of freedom: +X, -X, +Y, -Y, +Z, -Z
- And 6 rotational degrees of freedom:
- Clockwise around X- axis (CROT-X)
- Anticlockwise around X- axis (ACROT-X)
- Clockwise around Y- axis (CROT-Y)
- Anticlockwise around Y- axis (CROT-Y)
- Clockwise around Z- axis (CROT-Z)
- Anticlockwise around Z- axis (CROT-Z)
- To make sure the proper fixing of part we need to restrict all 12 degrees of freedom of the workpiece. The major portion of time of BIW fixture designer spent to deciding how to fix these all of DOF.
- The jig and fixture are tools to used for holding the workpiece in a correct location for mass production. Various types of fixtures are used in industry. The 3-2-1 method is fundamental principle for all types of fixture design.
- Elaborate types of BIW fixture stations?
- BIW stations is the part of BIW assembly line. The BIW assembly line is divided into zones and these zones are again divided into stations. The BIW stations are further divided into following
- Tool stations
- Geo fixtures: -
- In geo fixture tack welding done for all the parts to be assembled in that fixture. The geo fixture defines the geometry of a part.
- Re-spot fixture: -
- In re-spot fixture remaining tacks are completed.
- Re-spot fixture also have very tight positional technology. Re-spot jig pin tolerance will be 0-28 mm.
- Marriage fixture: -
- As name suggest the marriage of the different assemblies is carried out in this fixture.
- A different zones of assembly lines different assemblies are completed like under body, side body, front body, rear body etc.
- Framer fixture: -
- Framer fixture is next station after the marriage fixture.
- In framer fixture the roof is attached to the output of the marriage fixture and it form like frame hence it is called as framer tool.
- Checking fixture: -
- These are used to check the assembly parts, tolerance, dimension, and coordinates.
- It can be gauge type, fic type or automated checking fixture.
- Gripper stations
- A gripper is a device which enables the holding of an object to be manipulated. The easier way to describe a gripper is to think of the human hand. Just like a hand, a gripper enables holding, tightening and releasing of an object. A gripper is just a component of an automated system. A gripper can be attached to a robot or it can be part of fix automation system.
- Different type of gripper used in BIW as follow:
- Material handling gripper: - These grippers are used for material handling. These grippers can pick assembly from one station and will drop to another station.
- Process gripper: - These grippers are used to carry out some specific process like gluing, welding, riveting etc. in addition with material handling.
- Combo gripper: - Combo grippers are one which carry out multiple tasks like it can do material handling and also it carries out some specific process like gluing, welding etc. as well. Weld gun+ gripper
- Dual gripper: - These are two sided grippers. In case when we want one LH & one RH part, these grippers are used. It can handle material from one station to another. Gripper + gripper
- Stand stations
- Stands are used to hold part when not in use or also it is used to mount some parts or bodies on it.
- Different stands used in BIW
- Pedestal stands: - Weld gun is mounted on the fix stand which is mounted to the floor permanently. The gripper can carry the panel under the stand to do the operation.
- Gluing and sealer stand: - Gluing gun and sealer gun is fix to a welded or standard stand which is grouted to the floor permanently.
- Docking stand: - The robots have some limitations such as the play load capacity of the robot and also due to lack of space. When we select the robot for multitasking it can’t do both the task simultaneously due to limitations. In this kind of case, we add docking stand to put some equipment which is not in use for the current operation but will be required for next operation.
- Date stamp stand: - Every manufactured product has some data to stamp or to be embossed on it like serial no., batch no., date etc. for some future reference or for some data collection. The required data is stamped or embossed by using the stamping device mounted on the stand.
- Miscellaneous stand
- Curing: - After gluing it needs some time to cool down, so we put assembly on some belts & it will take the panel to another station & mean while gluing will cool down.
- Buffer stand: - After some operation we can put the no. of assemblies in this stand which is buffer stock & it can be transported to another station in easy way. They are also used to store the inventory while the machine is undergoing for some maintenance.
- Take out trolleys: - It used to take out some panels for inspection to rectify the process is going in right or not between the cycle.
- Conveyor: - Conveyor is the rotating path which transport the parts to the next station which are kept over it.
- What are the basic terminologies used in the BIW fixture?
- The following terminologies are used in BIW
- NC/Mylars/Fingers: - mylars is the component which holds the panels while operation. These are placed from top side & from bottom side also. The top side Mylars called as clamping Mylars & bottom side Mylars called as resting Mylars. Every clamping Mylars have resting Mylars. It doesn’t allow deformation of the part due to welding stresses.
- Principle Locating Point (PLP): - These are the points which are used for the accurate location of the part to maintain the geometry of the assembly. There are lots of holes on the panel which are not accurate due to stamping operation. the positional dimensions or relative dimensions are very precise in stamping & in fixtures also.
- Risers: - Risers are of different type like L-type riser, square tube riser etc. Risers is the manufacturing part which gives height to the assemblies.
- Blade: - Blades are plates mounted on the riser. Other parts like cylinder, arms etc. are mounted on the blade.
- Shims: - Shims are the small part which comes with the thickness of 0.1mm, 0.2mm, 0.5mm, etc. These will compensate the stack up tolerance which reflects at the panel holding part called Mylars. We give tolerance to all the parts of the fixture. Due to this tolerance the Mylars will either lift up or goes down from its defined position.
- Rough locators: - The operator can place the part in wrong orientation mistakenly. The rough locator will work as a guide while placing in the fixture & the part will be loaded in desired orientation. It is a parts of fool proofing.
- Hardware’s: - Hardware’s are like the hex head bolts, Allen bots, hex nuts, spring washers, self-locking nuts etc.
- CMM: - CMM stands for coordinate measuring machine. It is a device that measures the geometry of physical objects by sensing discrete points on the surface of the object with a probe. It generates report my comparing the data with CAD file data.
- Unit: - The fixture is the assembly of different types or units to form a fixture. There are different units like pin unit, base unit, clamping unit etc.
- Number plates: - Number plate is the aluminum embossed plate placed on each unit for easily recognizing the unit.
- Name plate: - The data like manufacturing company name, fixture name, fixture weight etc. is embossed on the plate & joined to the fixture.
- Clamp arm: - Clamp arm is the part of clamp unit which moves over axis. Over clamp arm the Mylar are mounted.
- Pivot: - It is an axis about which the clamp arm will rotates.
- Class A surface/skin surface: - the outer panels of the car like hood, door, backdoor, fender, roof etc. are visible to the customer. The outer panels should aesthetically very good. No any scratches or dent is acceptable over it. While designing the fixture to the skin surface the clamping material should be soft, so that it could not able to left any impression or dent over skin. Generally, nylon or pu material used for clamping purpose.
- Reed switches & sensor: - These are the electric components used in automated fixtures. The reed switch is an electrical switch operated by an applied magnetic field. The defects the panel is loaded or not is one by sensors.