Week 1:- Introduction to BiW and Fixtures Challenge
1 - WHAT IS BIW AND DEFINE ITS PARTS ?
ANS -
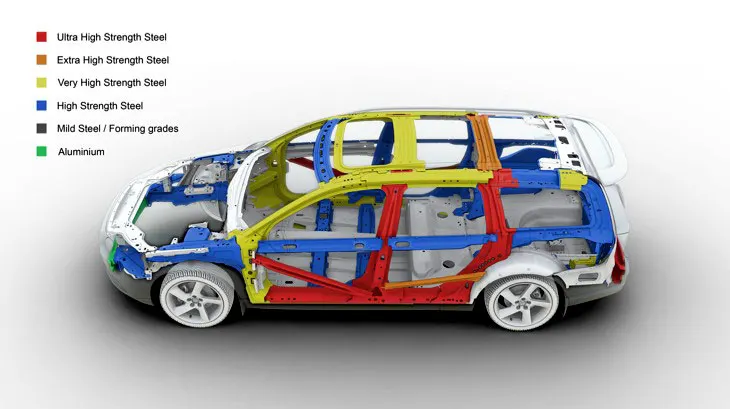
Biw or Body in white is the welded sheet metal components which forms the vehicle structure to which other components are married . It is a stage in automobile manufacturing in which the cars body structure is joined together that is before painting , motor, chassis, subassemblies or installation of trims . the assembly involves various techniques like welding (spot,mig,mag), riveting , clinching, bonding and laser brazing . In car design phase , biw is where the final contours of the body are worked out, in preparation for ordering of expensive stamping die .
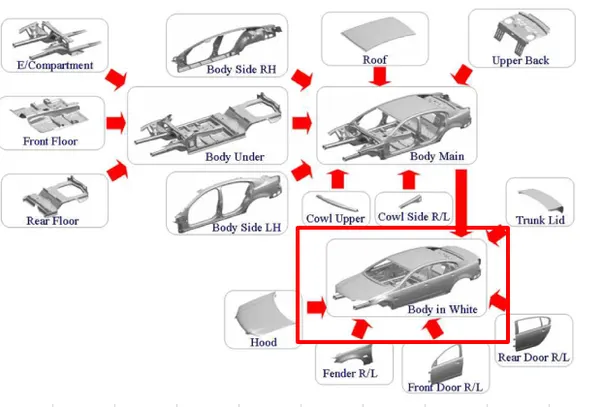
Biw is divided into various parts which is
- Body sides
- Underbody
- Closures
- Roof
- Fender.
Body sides has two parts body side outer and body side inner . under body is divided into three parts that is front end under frame , main floor and rear end under frame . the front end under frame is the engine compartment , main floor is the part where occupants will be and the rear end under frame is the rear compartment of the vehicle . closures include parts like front door , rear door , hood and decklid . the closures have inner panel and outer panels . roof has inner panel and outer panel . the process of joining will be like the under body parts will be first joined together , then the body sides will be joined to this structure , and simultaneously the inner panels will be joined to the corresponding outer panels . then this will be joined to the main structure .
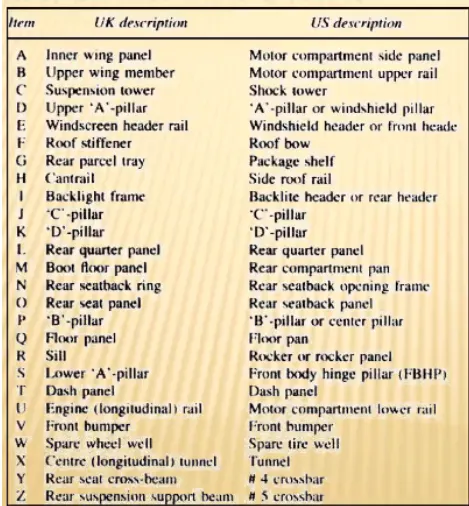
2 - WHAT DO YOU UNDERSTAND BY BIW NOMENCLATURE ?
ANS - Nomenclature is assigning names to a particular thing or a object . this nomenclature can differ from region to region even if the object is literally the same . similarly automobile industry around the world have nomenclatures for parts which differ from region to region . so below we will see the difference in nomenclature in UK and US.
3 - WHAT IS FIXTURES AND ITS TYPES ?
ANS - A fixture is a device which is used to hold the workpiece that is to be processed (welding, rivetting , etc) such that the workpiece does not get damaged during the operation . the fixture is built keeping in mind the 3-2-1 principle . the important task of a fixture is to hold the workpiece in place during the processing such that the geometry of workpiece is maintained and not damaged .
Biw fixture is of three types -
- Production fixture - Production fixtures as the name suggest is used for production purpose . it is basically a mass production fixture . since it is used for mass production , frequent maintenance of the fixtures is done . for this purpose the fixtures should be built such that it provide ease in maintenance .
- Pre production fixture - Pre production also known as PPO is a fixture that is used for initial batch production study . these fixtures are basically prototype fixtures which will check the tooling feasibilty of initial batch production . if needed modifications can be done on the fixtures .
- Checking fixtures - Checking fixtures is fixture which is used for the inspection purpose only. joining operations such welding , riveting , glueing etc are not performed on this fixture. various gauges are used in the fixture to check the dimension and tolerances of the part .
4 - WHAT IS THE BASIC PRINCIPLE OF FIXTURE DESIGN ?
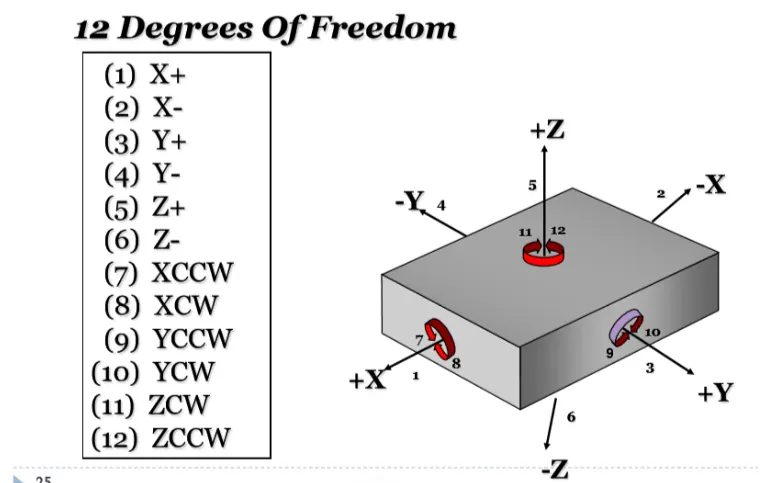
ANS - The basic principle of fixture design is to hold the workpiece firmly throughout its operation . every object has 12 degrees of freedom that is 6 translational and 6 rotational .the main objective while designing a fixture for a workpiece is that to make sure these 12 degrees of freedom of the worpiece is arrested , so the fixture is built in such a way that it will hold the workpiece in inplace firmly arresting the 12 degrees of freedom .
5 - ELABORATE TYPES OF BIW STATIONS ?
ANS - A Biw assembly line is where different types of panels are joined together in each specified zone , these zones will have different stations . below is the list of different type of stations -
a) Tools station-
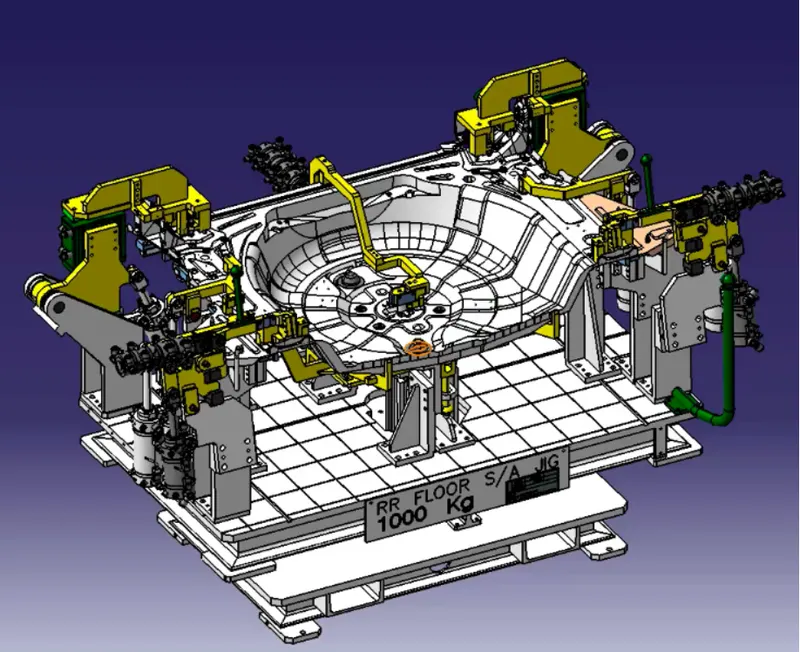
- Geo tool - It is a fixture in which the geometry of panels which are welded together is defined accurately . the pin for geo tool is of close tolerance that is -0.15 mm in general .
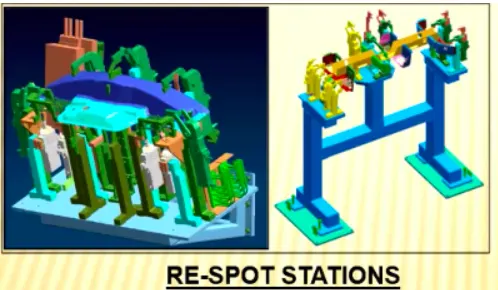
- Respot tool - It is a fixture which covers the remaining welding process which were left out or not covered in geo tool .the pin tolerance is -0.28 in general .
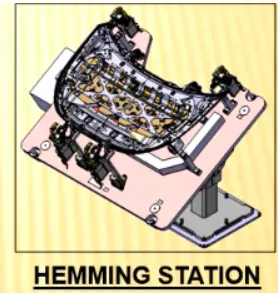
- Marriage/hemming tool - It is a fixture where the outer panel and the inner panel is joined together . this is mainly done on closure parts like hood , tailgate etc.
- Checking station - It is a fixture which is used tocheck the automotive parts and assemblies ensuring all coordinates , relative dimension , position as per the required tolerance . a checking station may be gauge type , fixed type , automated type .
b)Grippers station - It is a fixture which is used for holding purposes . it is fixed to manipulating end of robot or end effector known as EOAT (end of arm tooling) . there are types of gripper -
- Material handling gripper - It is used to handle car panel from one station to another .
- Process gripper - It is used to handle panel from one station to other station , and in addition to this it undergoes process like pedestral welding , pedestral rivetting , gluing , sealing etc .
- Combo gripper - It is type of gripper which is used for handling and in combinaion to that it has a weld gun on a side of this gripper for welding .
- Dual gripper - It is a two sided gripper which is used for handling from one station to other station .
c) Stands station - Stands are used to hold the parts when it is not in use and it is also used to mount some parts on it . stands are mounted firmly to the ground floor permanently .
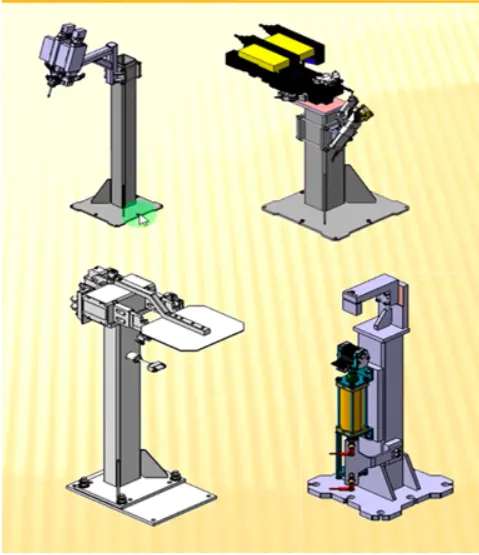
- Glueing and sealing stand - This stand has a glueing and a sealing gun on it and it is grouted to the floor permanently .
- Docking stand - When a robot has to do multiple task but it cannot hold all the tools , a docking stand is provided .
- Date stamp stand - For the parts that we make it is necessary to give them some identification for their easy callouts in future . so some details like date , serial no , part no etc is to be embossed on the part . this embossing is done by the tool which is mounted on the date stamp stand .
d) Miscellaneous station - These are the additional stations that is required in Biw assembly line .
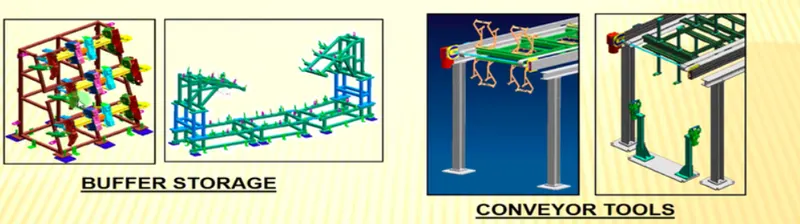
- Buffer storage - It is used to store the inventory while the machine is going under maintenance . it is also used to put some parts in buffer stock , and it is transferred to next station .
- Conveyor tool - It is used to transfer parts from one station to the next via a convevor chain or a conveyor belt .
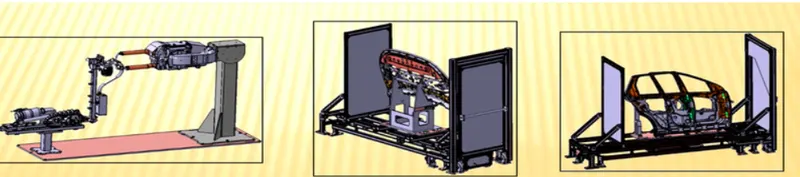
- Take out trolley - It is used to take the parts from the workingstations to the inspection station .
- Curing station - After the welding or glueing process , it take time for the part to be cooled , for this purpose curing station is used .
6 - WHAT ARE THE BASIC TERMINOLOGIES USED IN BIW FIXTURE DESIGN ?
ANS - There are many important terminologies used in biw fixture design which is given below -
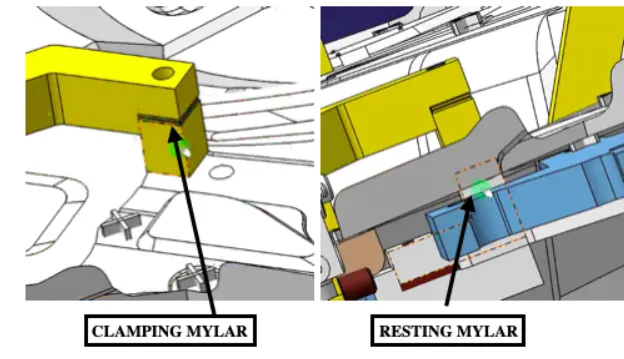
- Nc/Mylar/fingers - mylar is a tool which holds the parts . it is also known as nc block . there is two mylars , resting and clamping mylars . every fixture should have both resting and clamping mylars .
- PLP (Principle locating point ) - It is used for accurate location of part for maintaining geometry of assembly .
- Blade - It is a plate mounted on the risers .
- Risers - It is a part which gives height to the assemblies . riser can be of L type , welded square to frame type , etc .
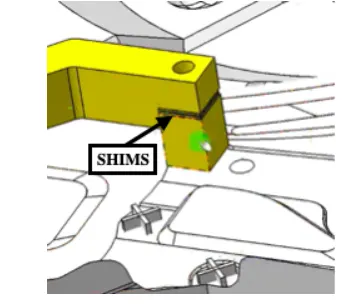
- Shims - shims is a tool which is used in adjustment for the stack up tolerance , this shim comes in various thickness .
- Rough locators - Rough locator is used as a guide locator so that the workpiece will not be incorrectly mounted on the fixture . rough locators are used in manual fixtue .
- Hardware - Hardware are nuts , bolts , screws , washers etc .
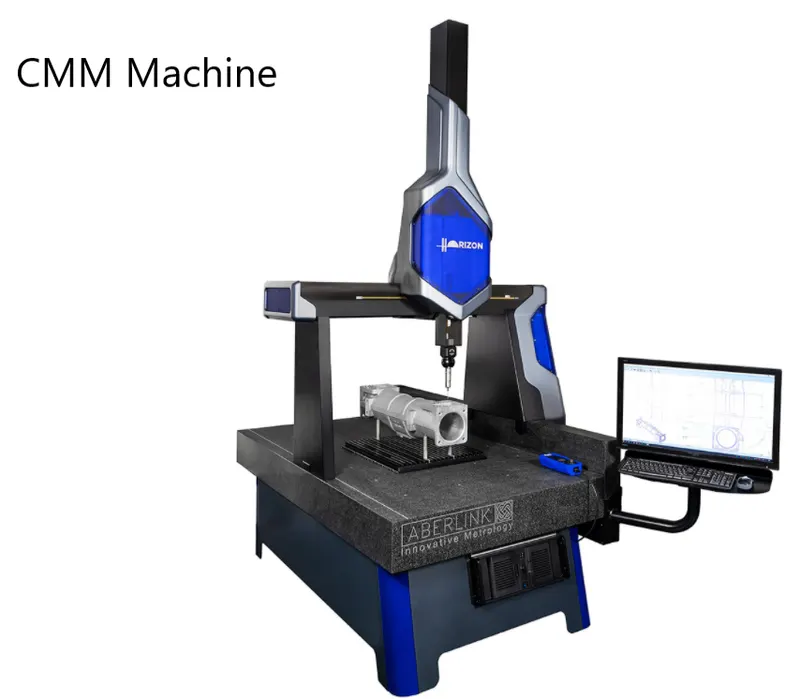
- CMM - It is a coordinate measuring machine which is used to measure workpieces precisely .
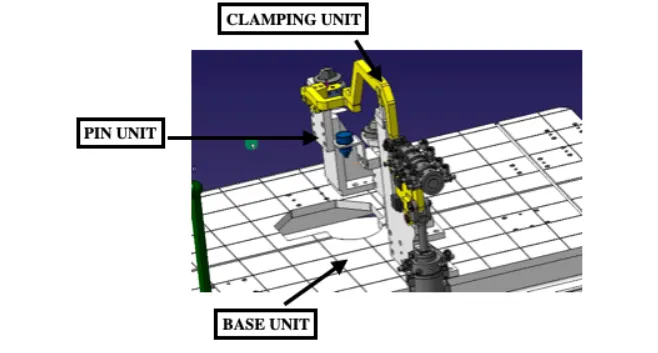
- Units - A fixture is basically formed of various components . this components are called as units .there are units like clamp unit , base unit , pin unit etc .
- Number plate - It is a identification plate for the units .
- Name plate - It is a identification plate for the fixture .
- Clamp arm - In the clamp assembly unit , the arm that moves is called clamp arm .
- Pivot - It is the axis around which the clamp arm will rotate .
- Class A surface/ skin surface - class A surface is the styling surface . this surface is visble to the customer so no damage should be done to this surface .
- Reed switches and sensors - It is a electronic device used in automated fixtures . It is used for detection of panel and automate opening and closing of clamp .