Week 1:- Introduction to BiW and Fixtures Challenge
- What is BIW & define its parts?
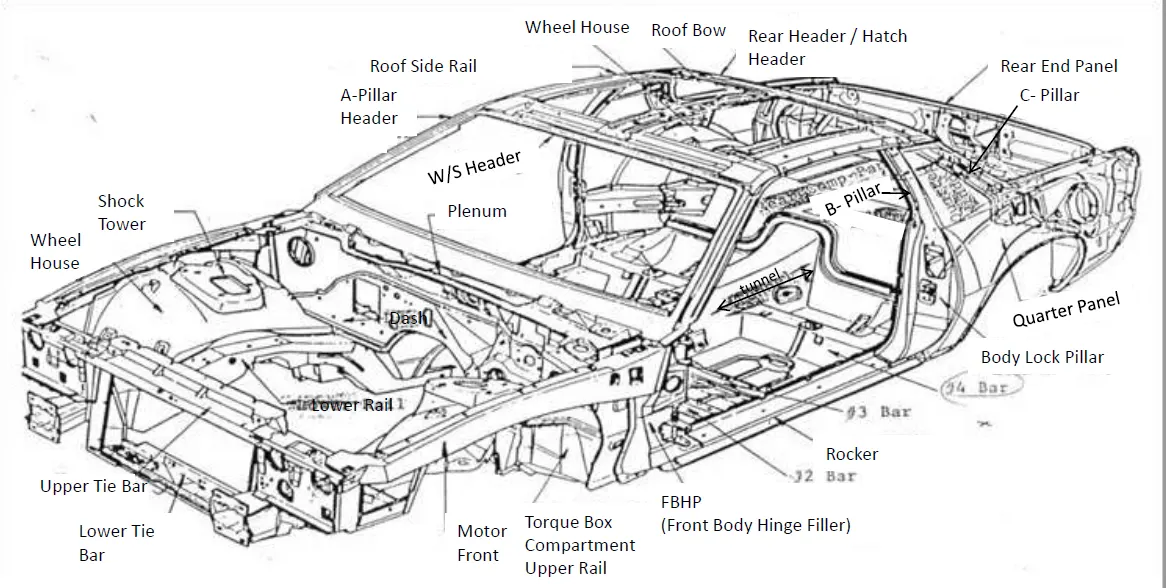
the stage in automotive design or automobile manufacturing in which car body sheet metal components are been assembled by welding and by other joining process.
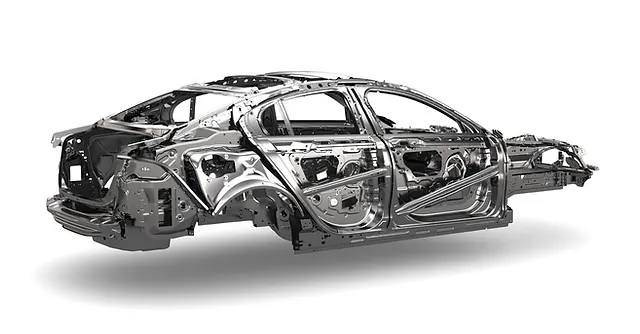
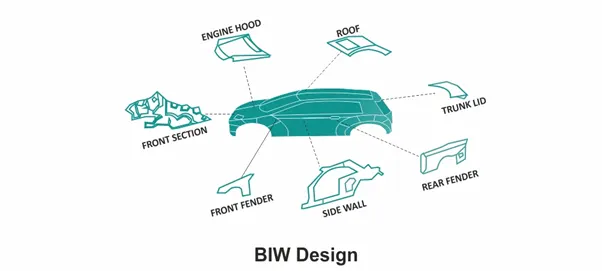
Biw parts are mainly categorized as below
body sides
under body
closures
roof
fender
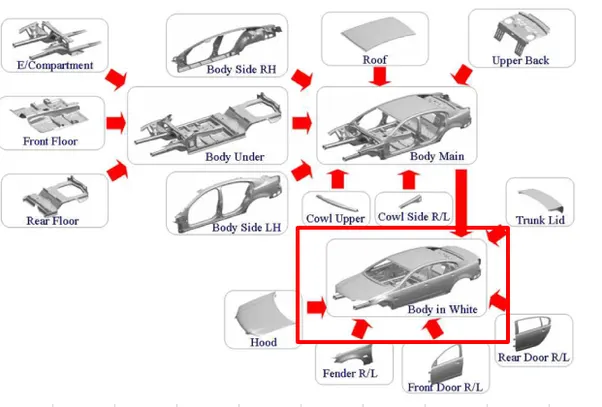
BODY SIDE consists of:
- Body side outer
- Body side inner
It generally refers to both the sides of the car that is left and right side. It mounts various BIW components like A-pillar, B-pillar, C-pillar, Panel side sill etc
UNDER BODY consists of:
- Front end under frame: This is the compartment are where the engine and other components of automobile like battery, radiator etc mounts.
- Main floor: This is the compartment where the interior parts like seats; infotainment panel etc will be mounted.
- Rear end under frame: This compartment shapes the rear end of the car. This is what provides space of mounting of rear closure parts and boot space.
CLOSURE components consist of:
- Front door: Two front doors on each side.
- Rear door: Two rear doors on each side.
- Hood: To cover the engine compartment.
- Trunk lid: To cover the interior and boot space.
ROOF consists of:
- Roof inner
- Roof outer
FENDER: The component seats between side body and front end under frame.
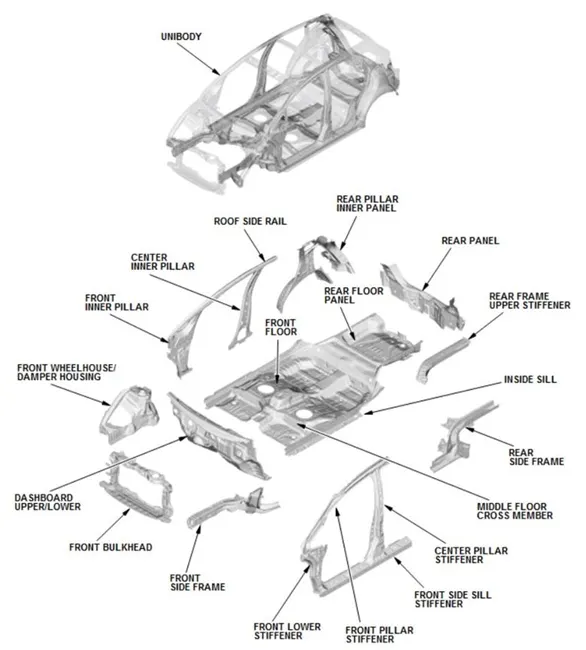
The below image shows precisely what a BIW of monocoque consists of
2 What do you understand by BIW nomenclature?
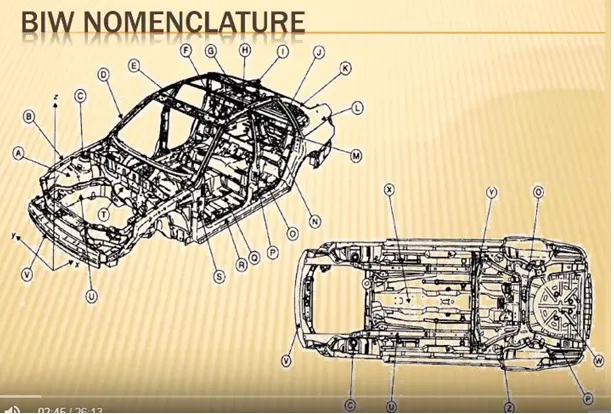
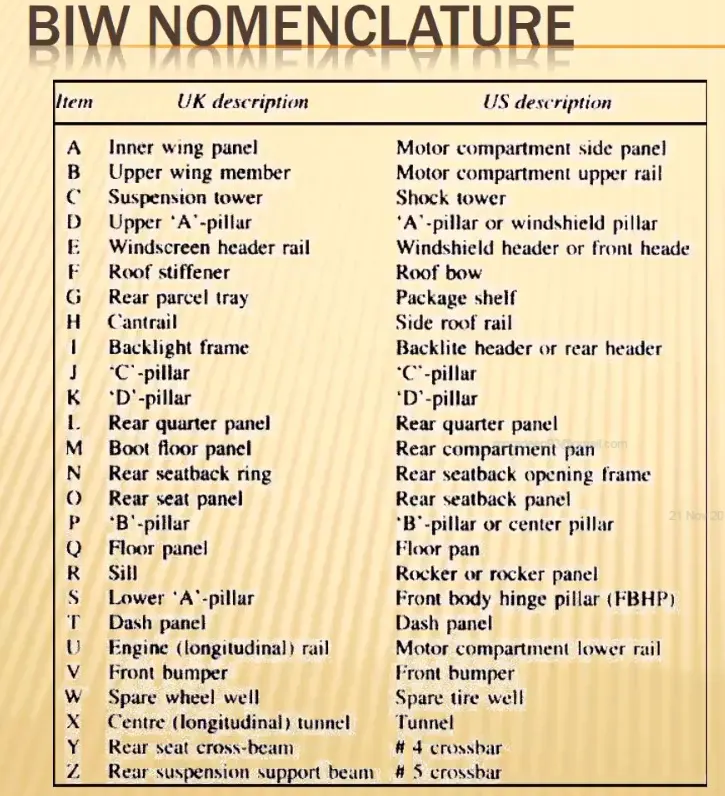
3 What is fixture & its types?
A fixture is a device which holds the work piece to be processed (welded) by using 3-2-1 principle
in generally a welding fixture (tool) consists of number of units together to hold the car panel, and is mounted on abase unit.
welding fixtures are normally designed to hold and support the various components (wok piece ) to be welded.it is necessary to support them in proper location which is capable of preventing distrotions in work piece during welding. for this the locatting elements to be places carefully, clamping elements has to be light but firm,placement of clamping elements has to be clear of the welding area and fixtures are quite suitable and rigid to withstand the welding stresses
types of fixtures
production fixtures: mass production purposes
pre production operating fixtures (PPO) : for initial batch production to study the feasability
checking fixtures: for car panel geometric inspection purpose
4 What is the basic principle of fixture design?
For a free body, there are 12 degrees of freedom considering the negative translations and rotations about their respective axis. To hold any part these DOFs need to be constrained.
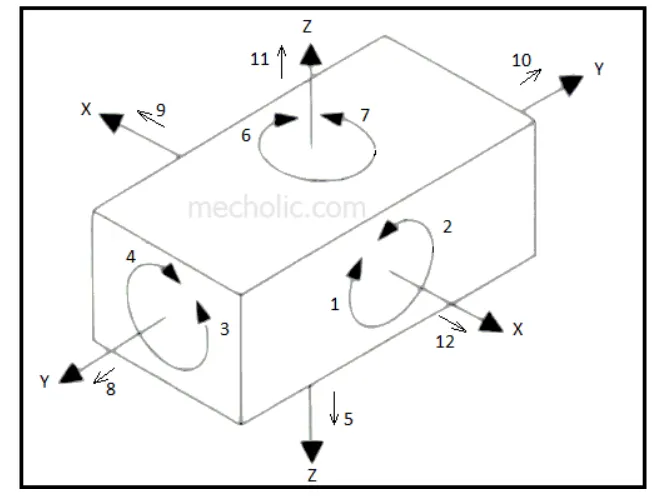
These are constrained by the 3-2-1 locating principle,
5 Elaborate types of BIW Stations?
work stations are categorized as fallows
1) tools
2) grippers
3) stands
4) miscellaneous
tools consists of
geo tool : a geo tool is fixture in which the geometry of the panels which are to be welded together is defied accurately. the pin tolerence for a geo pin will be of closer tolerence i.e: -015
for example
consider a panel hole size of 20 mm the pin diameter sholud be 19.85 mm
Respot tool:
a respot tool is fixture in which remaining weld spots which are not achieved in geo tool are welded for the pre weldding panel from the geo tool .
the pin tolerence for respot pin will be of tolerence with -0.28 in general.
for example
consider a panel hole size of 20mm , the pin diameter should be 19.72
marraige or hemming tool
a marraige or hemming tool is a fixture in which the inner panel assemblyand outer panel assembly are joined together
these are done by welding or by hemming in case of closure panels.
Grippers consits of
a gripper is a device or a fixture which holds the car panel , and is fixed to the manupulating end of a robot or an end effector also known as EOAT- end of arm tooling
Material handling grippers (MH): material handling grippers are designed for handling the car panel from one tool station to other tool station.
process grippers: process gripper are designed for handling the car panel from one tool station to other tool station , and in addition to that it undergoes process like pedestal welding, pedestal riverting,gluing,sealing etc...
combo gripper: combo gripper are designed for handling the car panel from one tool sation to other tool station , also with combination of weld gun at another side of the gripper for welding.
Gripper + weld gun
Dual gripper: dual grippers are designed for handling the car panel from one tool station to other tool station , with two sided griper
Gripper + Gripper
stands consits of
Gluing and sealer stand: gluing gun or sealer gun is fixed to a welded or a standard stand which is grouted to the floor permenantly
Docking stand: when robots are selected for multi tasking like material handling & welding which cannot arry both due to some limitations ( pay load capacity of the robot or space constaint) the robot will drop and pick the gripper or gun after completing the respective operation with the help of docking stand.
Date stamp stand : the panel will get the date embosed on to it , with the date stamping decive mounted on this date stamp stand .
pedestal gun stand: weld gun is mounted to a fixed stand which is grouted to the floor permenantly , where the process gripper carries the car panel to weld the spot with this fixed weld gun.
Take out trolley: take out trolley id used to take the car panel of robotic working cell between cycle of inspection purpose.
6 What are the basic terminologies used in the BIW fixture
Basic terminologies used in the BIW fixture are
1 NC/MYLARS/FINGERS
2 PLP
3 BLADE
4 RISERS
5 SHIMS
6 ROUGH LOCATORS
7 HARDWARES
8 CMM
9 UNITS
10 NUMBER PLATE
11 CO-ORDINATE PLATE
12 NUMBER PLATE
13 CLAMP ARM
14 PIVOT
15 CLASS A SURFACE / SKIN SURFACE
16 REED SWITCHS
17 SENSORS.