Week 1:- Introduction to BiW and Fixtures Challenge
Introduction to BiW and Fixtures
1) What is BIW & define its parts?
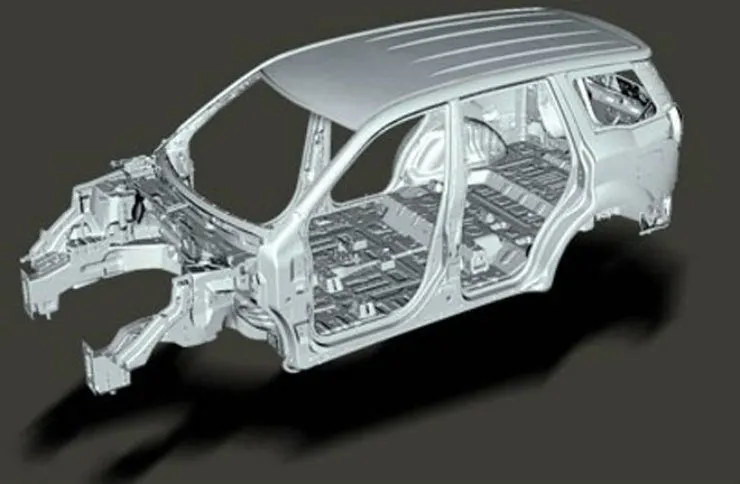
BIW term stands for Body In White
It is the stage in automobile where body shell structure sheet metal components are
welded together in weld shop just before painting
Why it is called white, while it is grey in color as a primer
In early years car shell structure were kept in white color
before assembling suspension, engine. It is kept white to give a color choice to
customer. Now term remains the same and refers to the welded sheet metal
structure.
BIW design is always driven by aesthetic, aerodynamic and cost criteria.
Parts of BIW
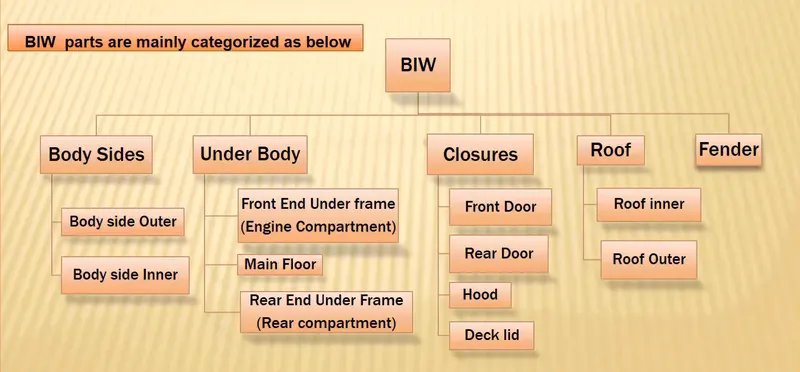
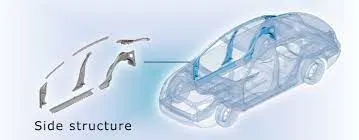
Body Sides :
* Body side outer - It is oustside main frame of automoble
* Bpdy side inner - It is a inside mainn frame of automobile
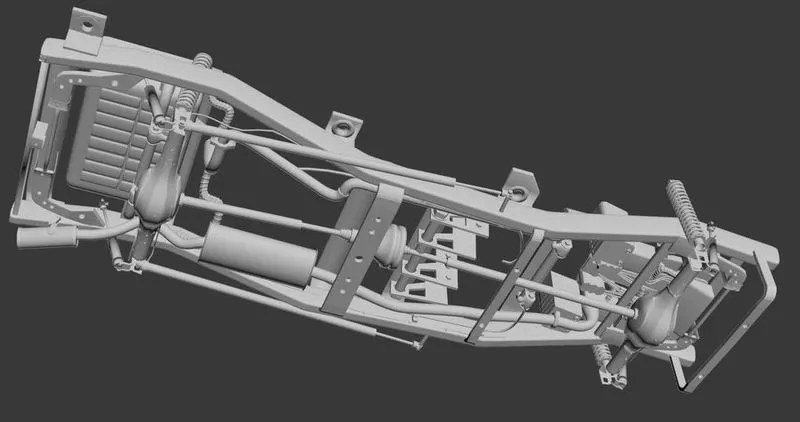
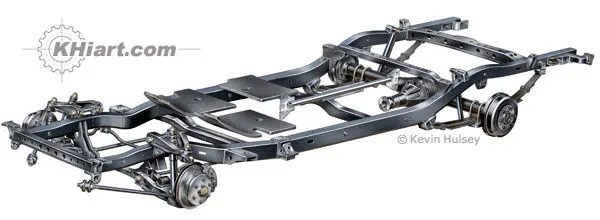
Under Body :
* Front end under frame - This consist of engine and other importnat
assembly holding area.
* Main floor - this main flor holds seat stand and other equipment.
*Rear end frame - Rhis end frame consist place for back space area and in
some cases for back seat area also.
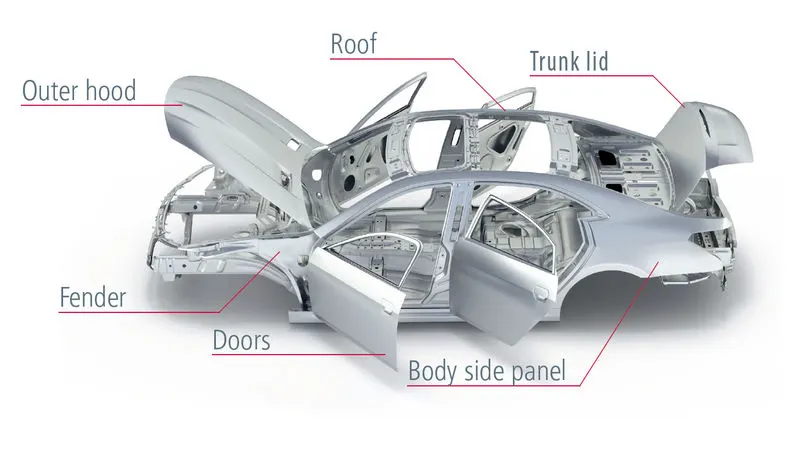
Closures :
* Front door - These are two front doors of a car.
* Rear door - Thease are two rear doors of acar.
* Hood - This is a assembly of cover to protcet engine compartmet and
also for pdestial safety criteria.
* Deck lid - This refers to the closure lid of the deck of the automobile.
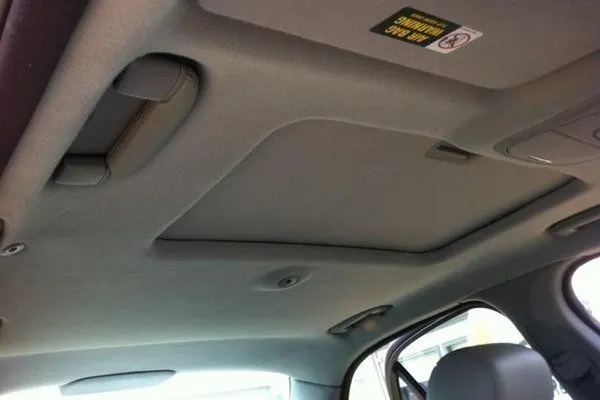
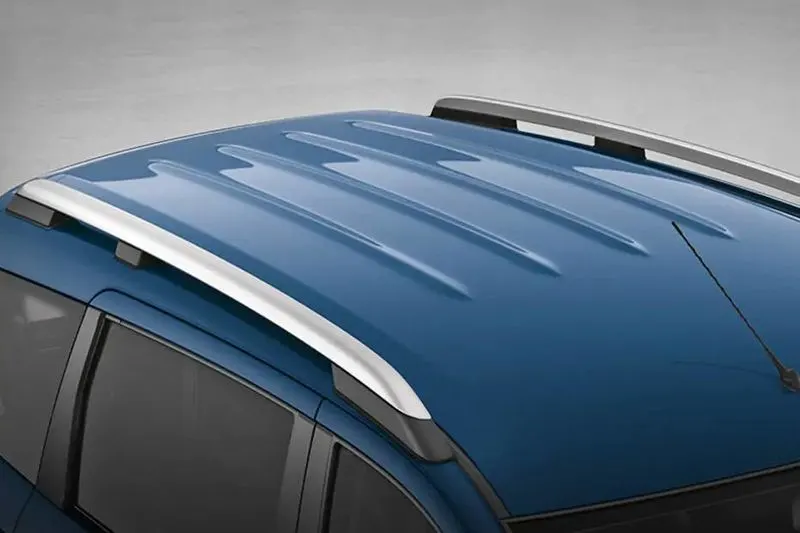
Roof :
* Roof inner - Roof inner which protect a car from inside. and this consist of inner lightining system & etc.
* Roof outer - this top outer cover of car which protects a car from outer side from
sunlight, rain and fromm many more.
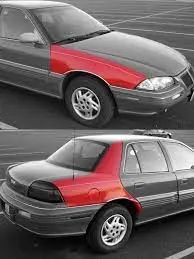
Fender :
* There are four fenders in a car like, Front left and right fender.
Rear left and right fender.
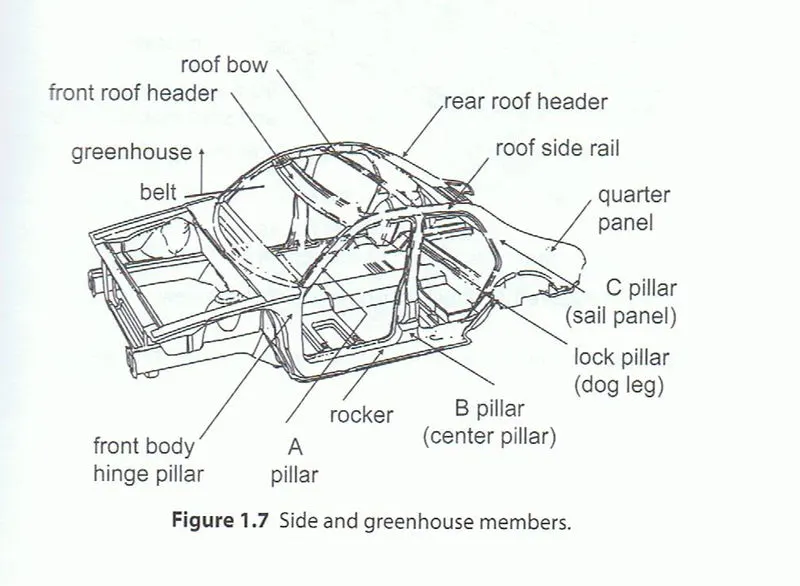
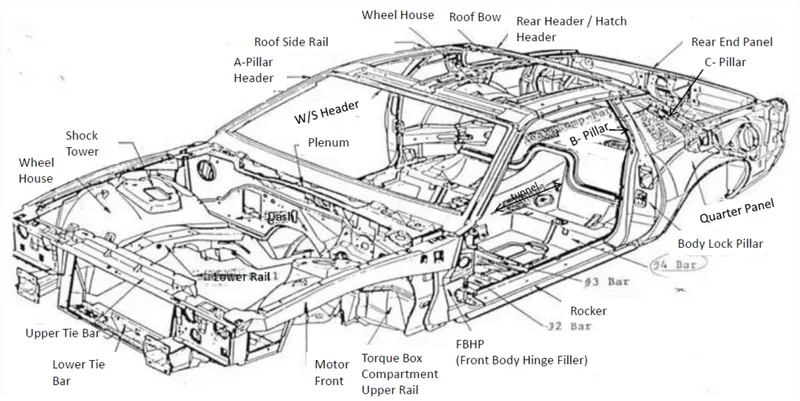
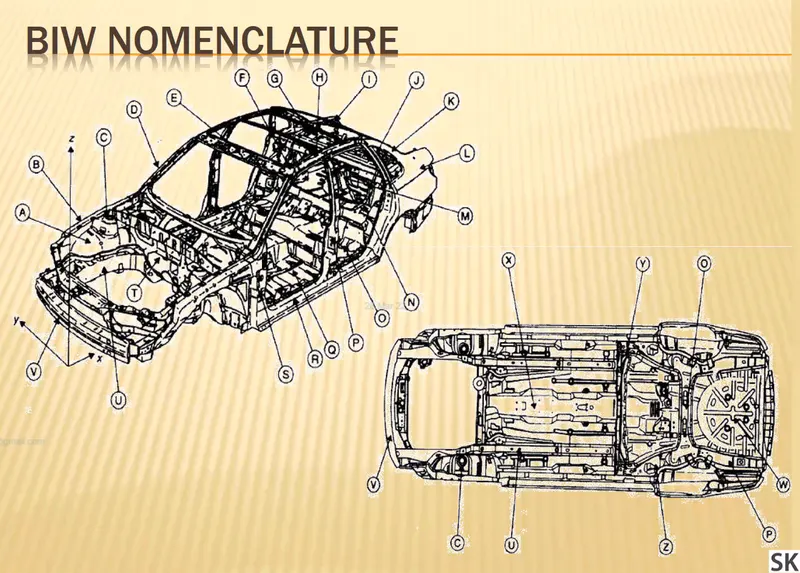
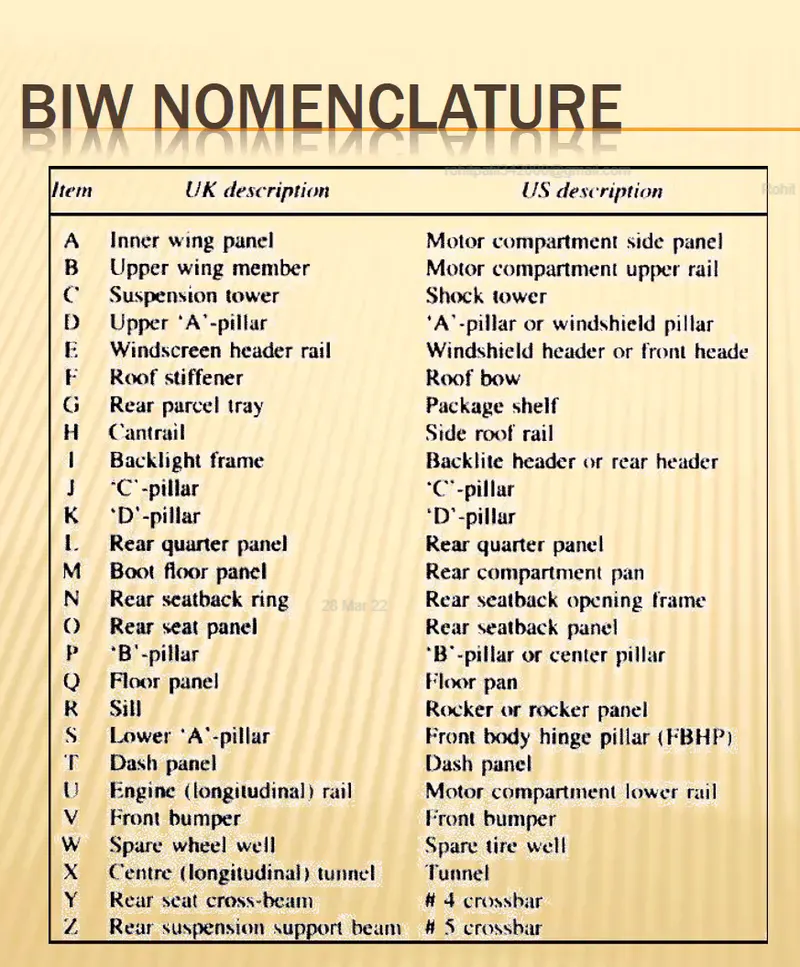
2) What do you understand by BIW nomenclature?
The nomenclature of BIW is simply useng names for on that perticular assemby.
This BIW assembly has made up of with so many diferant parts those parts
are we genarly call by their own name.
Then names of those parts, As given below.
3) What is fixture & its types?
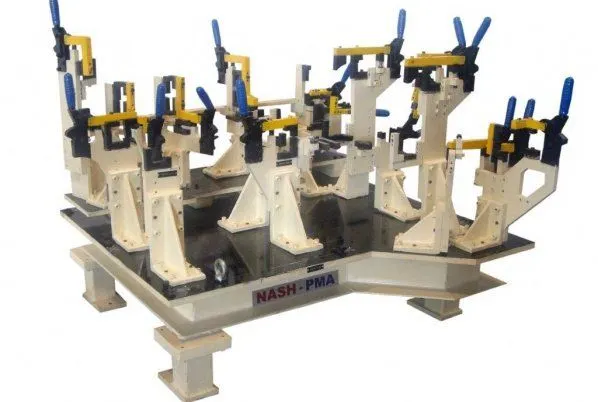
Fixtures provide a means to reference and align the cutting tool or welding to the workpiece
but they do not guide the tool.
It provides only a reference surface or a device. What makes a fixture unique is that
each one is built to fit a particular part or shape.
The main purpose of a fixture is to hold a workpiece during operation or some other industrial process.
Fixturing devices include
* Various standard clamps, chucks, and vises.
* Metal plates containing dowel and/or tapped locating holes or key slots.
* Dedicated fixtures with specific design and build requirements.
Types of BIW Fixtures -
1) Production Fixtures - Production fixtures are use for mass production. this will be done after trials only.
these type of fixtures made with harden material must so that we can achive that
acuracy till end parts, upto required target quanity.
2) Pre-production opertaion fixtures(PPO) - These type of fixtures are made for take trials of assembly
to check the fesibility for production. in this stage so many
trial and errors san be done by engineers to get final
desired ouput for production quantity and quality.
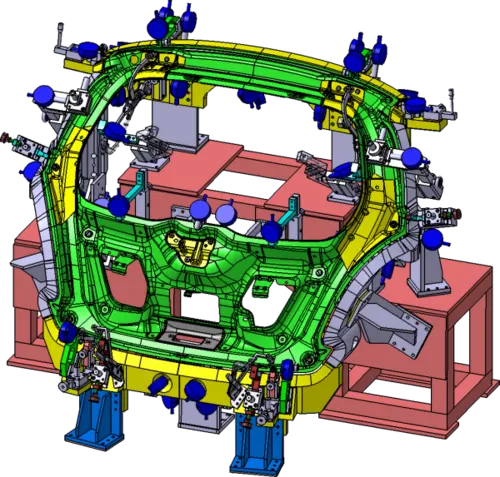
3) Checking Fixture - Checking fixtures simply we can call as quality fixtures, because of tese types of
fixtures are used for quality check. In this fixture all parameters are checked neatly
including all dimensions, geomatrics and all other parameters.
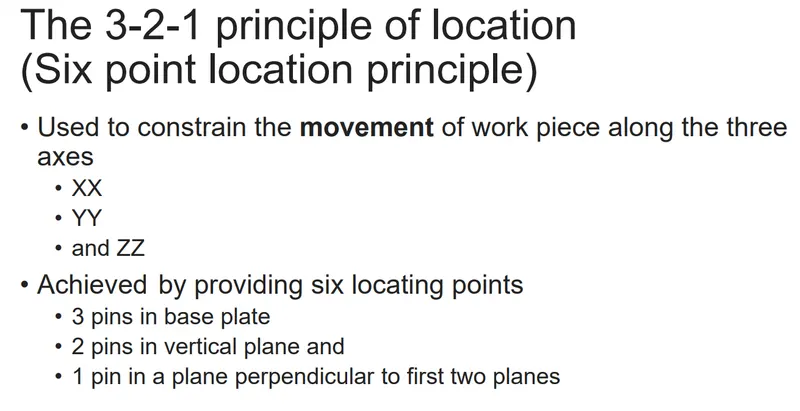
4) What is the basic principle of fixture design?
3-2-1 Principle
5) Elaborate types of BIW Stations?
BIW stations are nothing but part intigral part of BIW assembly line.
These stations are devided into deferant types as given below.
1) Tool stations
2) Gripper stations
3) Stand station
4) Miscellaneous stations
1) Tool stations :
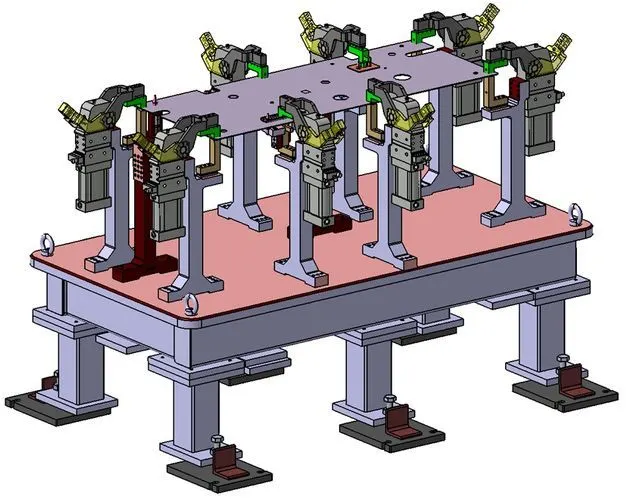
a) Geo-Fixtures - geo fixtures are used to maintain geomatric dimensions
in this stage of welding only spots are given to body.
In this accuracy is maintened for fixture machined parts = ± 0.02 mm
And for pin positional accuracy must be within -0.15 mm.
b) Re-Spot fixtures - As its name shows it is a Re spot fixture, on which previously given
some spotes to maintain geomatic dimensions in this accuracy is very tighter
like accuracy of Re-spot jig pin tolerance will be -0.28 mm.
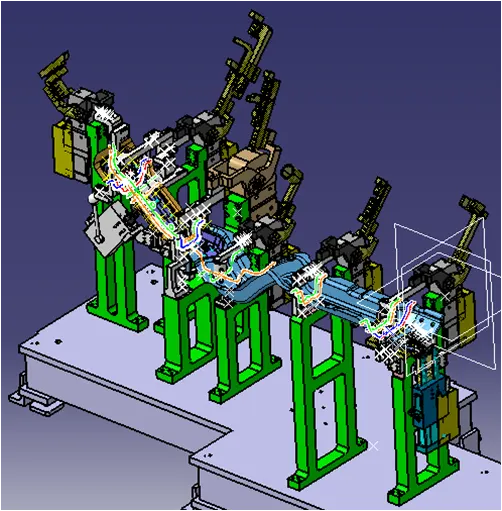
c) Marriage fixtures - As its name shows, In this fixture all parts like Under body, outer body, inner body
main chessy and other parts assembled together by joining methods,
Like Welding, brazing, Hemming, gluing and etc..
d) Framer fixture - This fixture is ntext to marriage fiture.
In this a roof is attched to the end of marriage fixture and then it will form
like a frame.
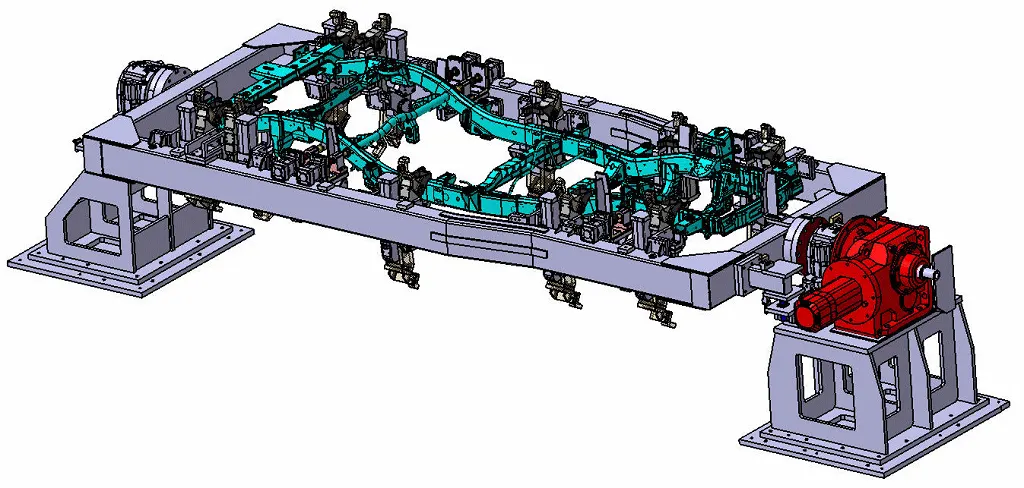
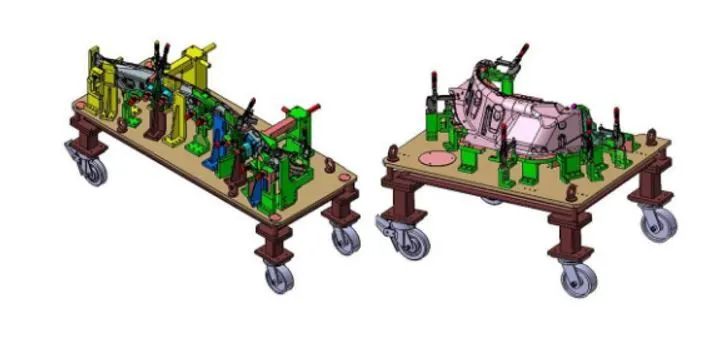
e) Checking fixtures - This fixture is used to check all the parameters,
Geomatric dimensions, check by using deferant gauges.
Checking frequency is depend upon quality and required target quantity of a lot.
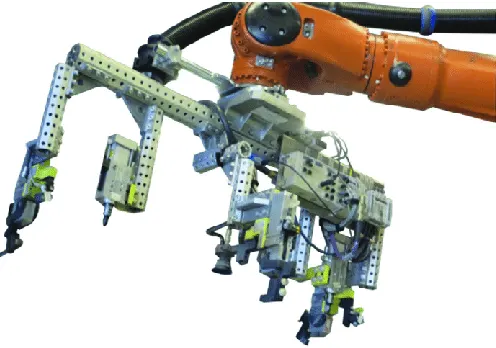
2) Gripper stations :
a) Matrial handling grippers - as its name shows it is used for material handing.
these are some time auto oparated by PLC and pnumatic controle
these acts like human hands.
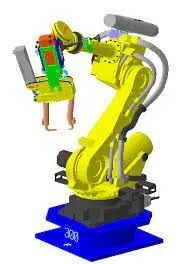
b) Process grippers - By these grippers we perfom some process like hemming, glueing, welding etc.
c) Combo grippers - These grippes made for perform muti tasking, by these grippers we can perform
Material handling and as well as preoss also.
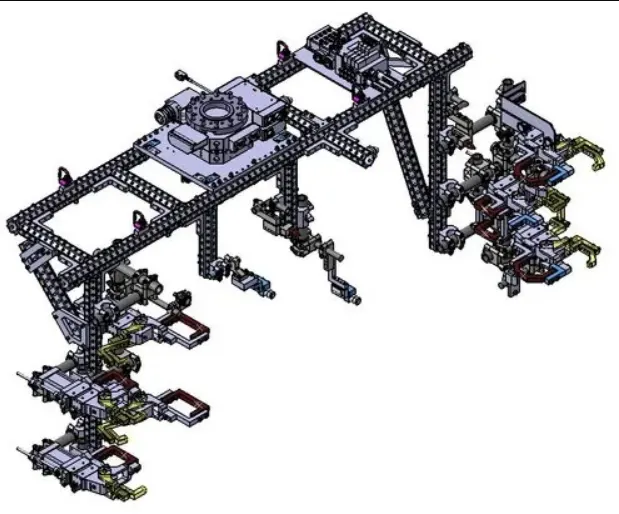
d) Dual grippers - In this arm is on both side LH and RH so we can produce assembly faster.
in these arm is connected both side and both arms will perform same time
it increse efficieny and decrese cycle time of process.
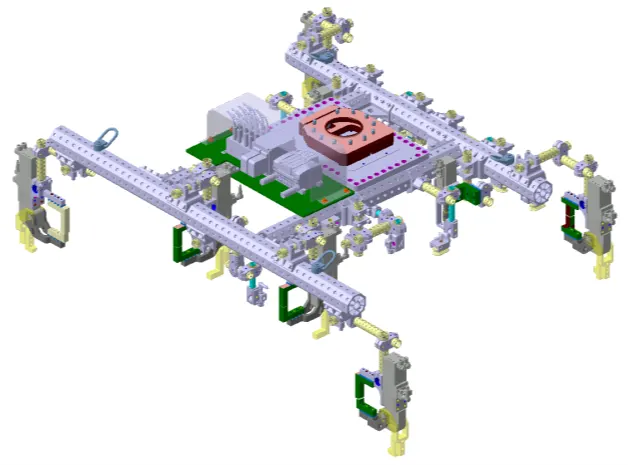
3) Stand stations :
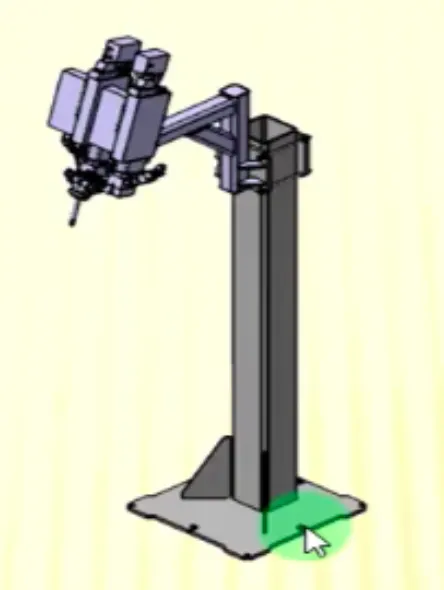
a) Pedestal stands - This Pedestal stand is fuxed on ground, in this one gripper welding gun is mounted this carries
welding operation by fixed welding gun.
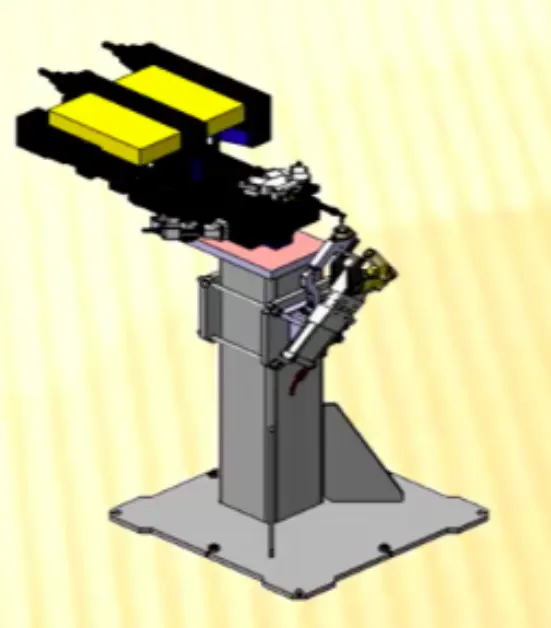
b) Gluing stands - As its name shows it is a gluning stand in which we do gluing operations while
attaching varies parts
c) Docking stands - This stand simple ditibute the the operation by Pickup and dropping operation,
For Ex. while performing welding process by one robot that same robot can not do gluing
on same time, where we use docking stand this will hold the welding until gluing compeltion.
after completeing it it return the welding gun for operation.
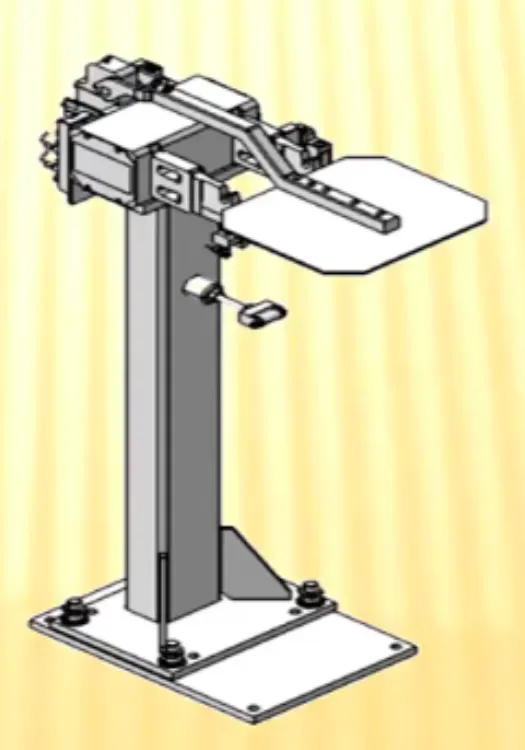
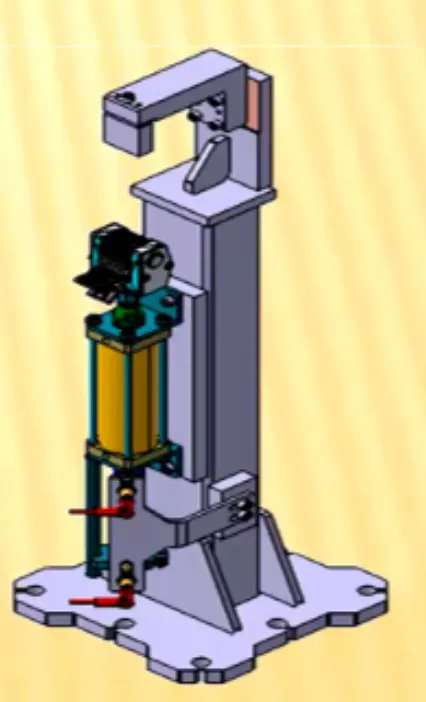
d) Dtae stamp stand - This is pnumatic operated stand in which date and some time manufacturing data will
stampped in the form of embossing.
4) Miscellaneous stands :
a) Curing - After gluing operatin asseblu has to be cool, so that we put on acuring line.
It is simplu a trolly or coneyor system
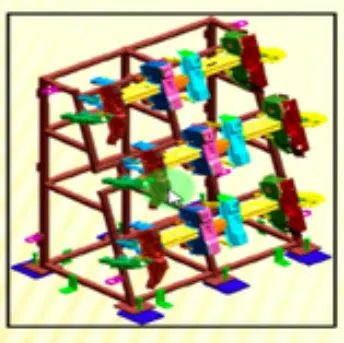
b) Buffer stand - In a larger assembly line, cycle time of assembly for all parts can not be same.
Some part will assembled faster and some of them slower, so to maintain the
line running and sycronize we keep some fast moveing parts in strok
To keep them in stock we generaly use Buffer stand.
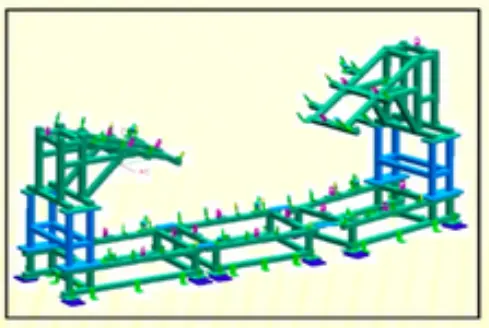
c) Take out trolleys - These trolleys are used to take one part from running assembly line for inspection
purpose. thats why we call it as aTake out trolleys.
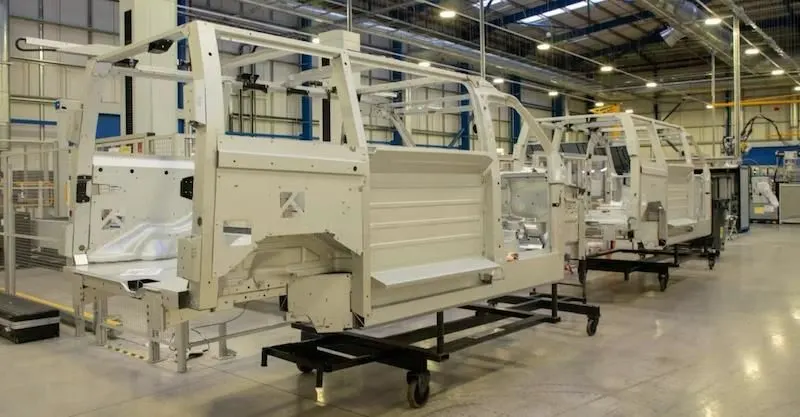
d) Conveyors - These are general conveyors, Used for aseembly and parts movement from one station to
another station without any time loss and damage.
6) What are the basic terminologies used in the BIW fixture?
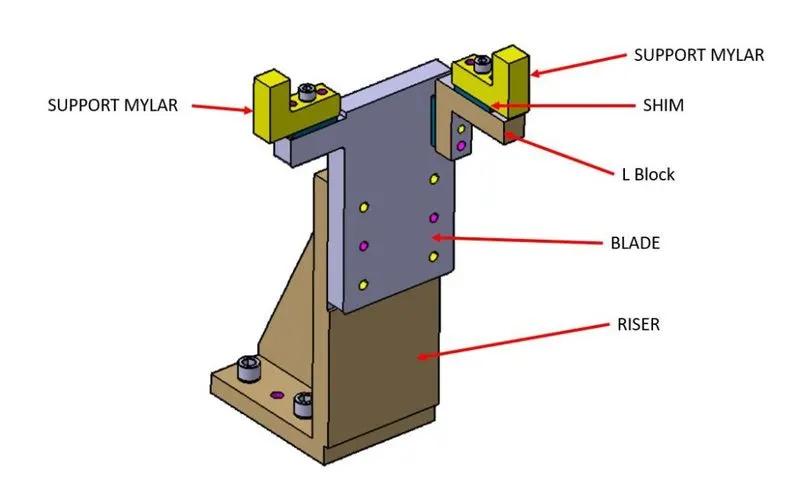
a) NC/Mylars/fingers - Mylers/Fingers these holds the panel to perform operation
in this two types - 1) Clamping mylars
2) Resting mylars
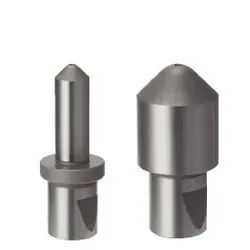
b) PLP (Principal Locating Pins) - These pins are locating pins used to achive locate the pane
to achive quality and quanity repitabality in all the processes.
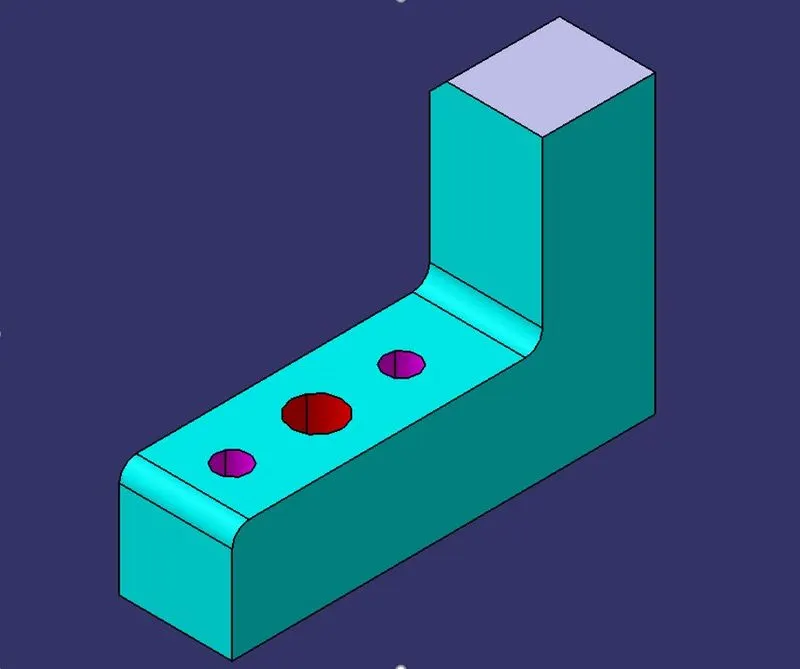
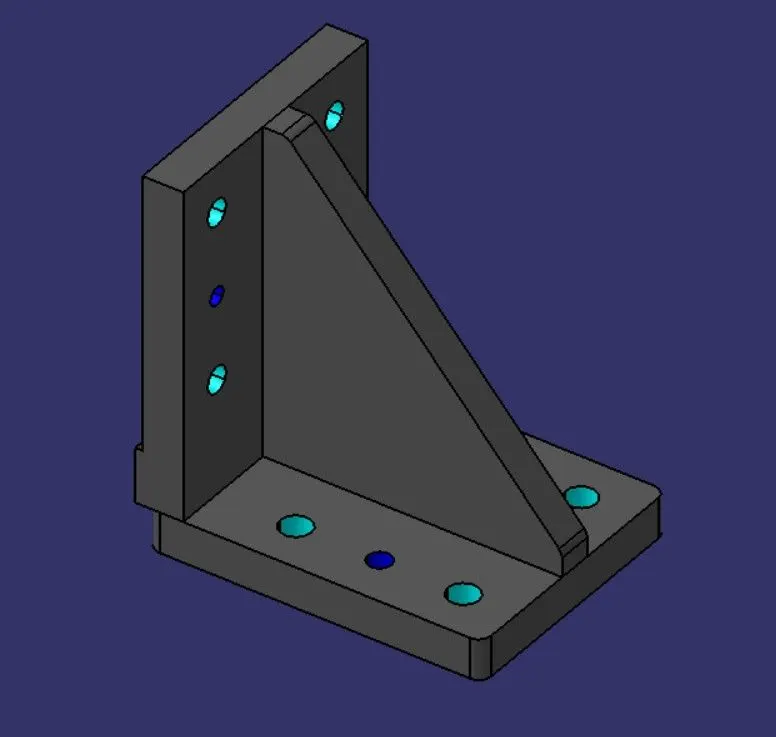
c) Risers - There are like L type frames used to maintain height of grippers and all in a fixture.
d) Blades - These blades are mounted on risers to hold assemby of pin, cylinder and etc.
e) Shims - Shims are thin sheets thickness of 0.2 to 0.5, Used to adjust height of mylars and grippers and holdings.
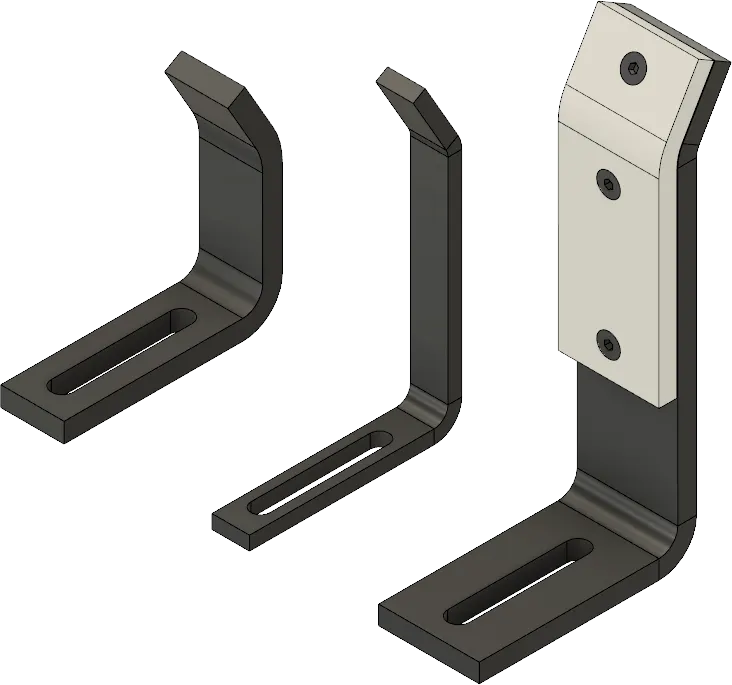
f) Rough locators - these are simply locatros so that operatos can understand where he have to place the panel.
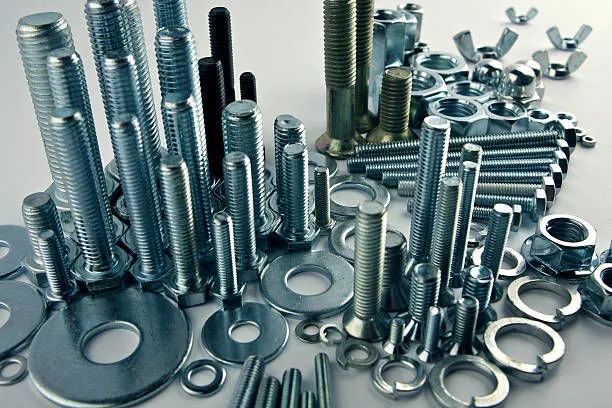
g) Hardwares - We use hardware components in a BIW fixture like nuts. bolts, studs, fastners, washers and etc.
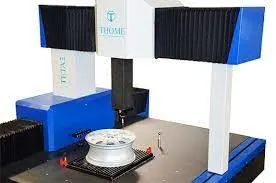
h) CMM - co-ordinate measuring machine this is a quality measuring machine of any kind of component
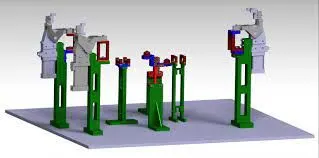
i) Units - In a BIW fixture number of units are there like pin unit, clamp unit, base unit and etc.
j) Number plate - This number plate is Number embossed alluminium plate attached on each and every
unit of BIW fixture to recogonize the unit and its details. and for easy identification.
k) Co-ordinate plate - in this a single hole has done to take reference for all other holes.
l) Name plate - This is also a embossed alluminium plate attached front of BIW fixture,
on this plate all details are writen like name of manufacturer, date , capacity,
material and other important genara data.
m) Clamp arm - As its name shows this clamp arm is responsible ber clammping of panel while
during operaions.
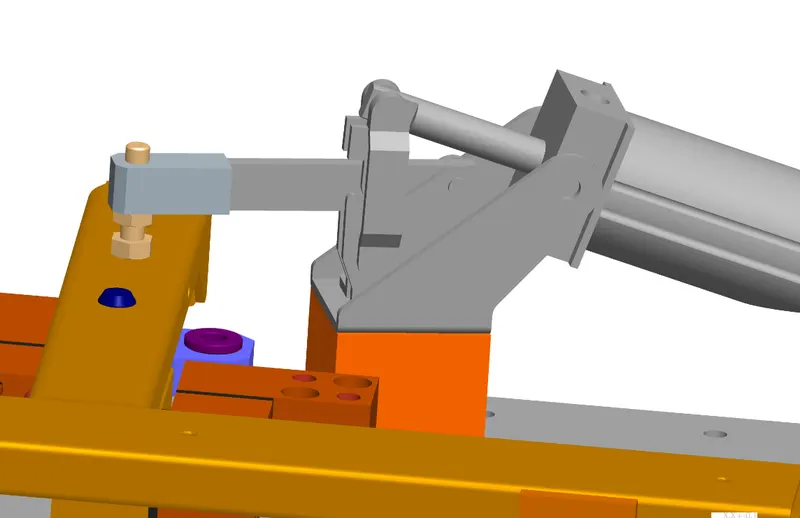
n) Pivot - This pivot is elmennt about which the clamp arm swivels.
o) Class A surface - Class A surface is a surface of car body which is visible to end customer,
so on this surface we have to hold very softy while performing operations
to avoide dents, cracks and holding martks.
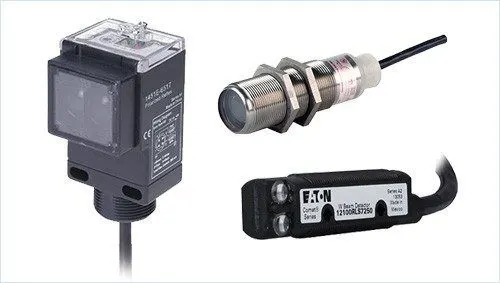
p) Reed switches and sensors - In a automatic BIW fixture to perform automatic operatins like clamping,
unclamping, moving, welding, gluing and etc., there is requirment of sensors,
switches which must for a any automation system.