Week 1:- Introduction to BiW and Fixtures Challenge
1.BIW abbreviates Body In White, which nothing but a core shell structured form of sheetmetal components in automobile manufacturing industries as before going to painting.
OR
BIW(Body In White) is a stage of Design or Manufacturing in automobile indusries,in which all the sheetmetal parts are assemble or join together(Welding,Riveting..) to form a core shell vehicle structure where other components are mairred(Engine,Interior Trims,Chassis...)
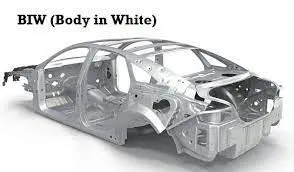
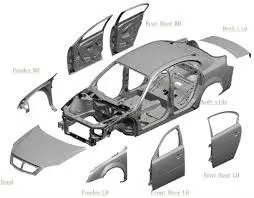
Parts of BIW as follows:
Body Sides:
- Body side outer: This refers to the outer L/R side of the vehicle body parts.
- Body side inner: This refers to the inner L/R side of the vehicle body parts.
Under Body:
- Front End Under Frame: This refers to the frame under the bonnet(Engine compartment.)
- Main Floor: This refers to the middle part of frame where seats are mounted.
- Rear End Under Frame: This referes to the rear part of frame(Rear compartment.)
Closures:
- Front Door: This refers to the parts of front door panels of the vehicle.
- Rear Door: This refers to the parts of rear door panels of the vehicle.
- Hood: This refers to the closure door of vehicle to cover Engine.
- Deck Lid: This refers to the closure door of vehicle main laggauge comp
Roof:
- Roof Inner and Outer: This refers to the inner and outer side roof surface of a vehicle.
Fender:
- This refers to the frame of a wheel in vehicle as well.
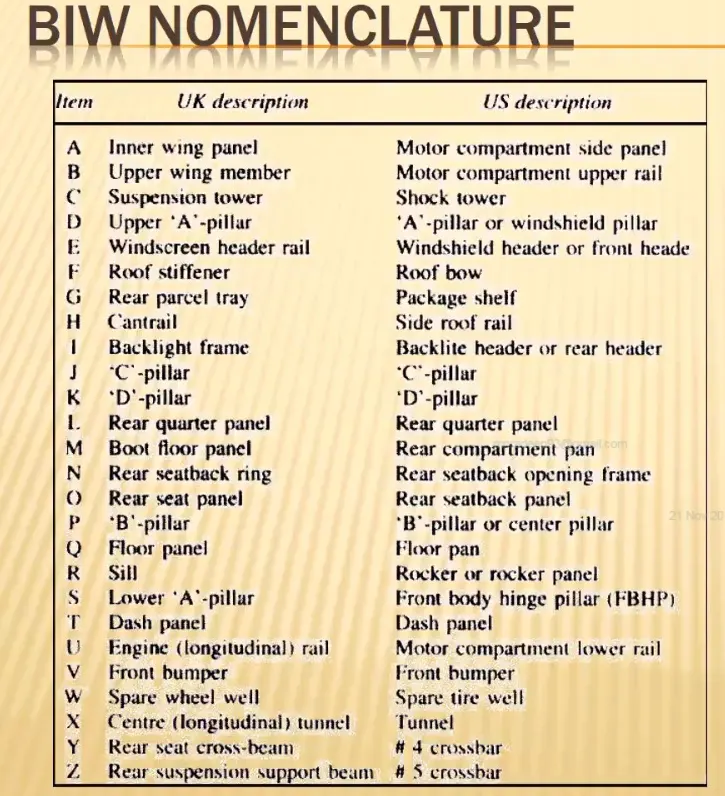
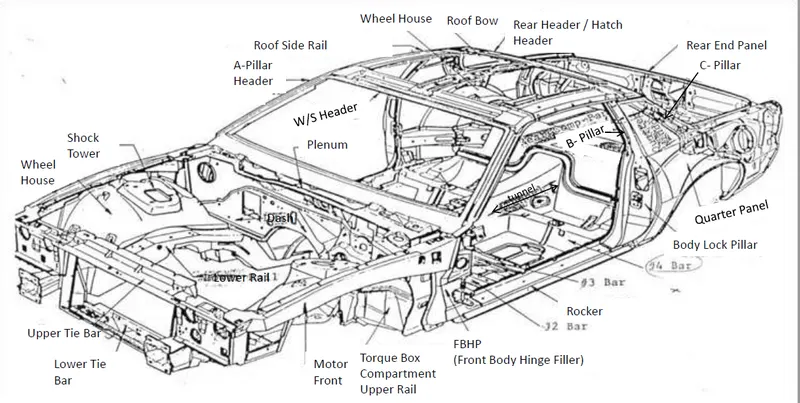
2. BIW(Body In White) structure involves with several parts.Basically to identify these parts UK&US are given part names accordingly are called BIW Nomenclature.
Some of the common Nomenclature to idetify parts are given below.Both are represent name of same parts/components in BIW Nomenclature.
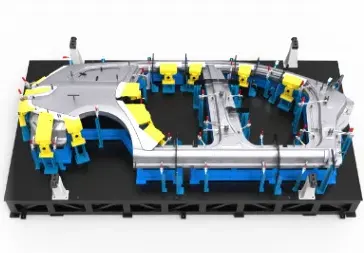
3. In general a fixture is a holding & supporting device which is designed by 3-2-1 principle without cause any vibration,Distortion or stresses in the workpiece.It ensure proper location,minimize part handling and error proofing during production run.
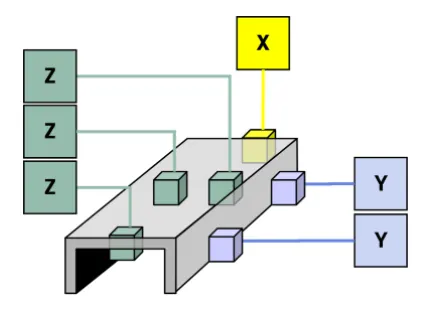
The 3-2-1 Principle is a component holding principle where 3pins are located 1st principal plane i.e xy,yz,zx. 2pins are loacated in 2nd plane which is parallel to 1st plane and one pin located in one plane mutually perpendicullar to 1st/2nd planes.
Types of Fixtures:
Production Fixtures
These fixtures are used for mass production purpose.Considering mass production these fixtures should design simple as well as easy to maintainance purpose so that cycle time,workpiece loading/unloading and productivity goes up.
Pre-production Operation Fixture
This fixture is the base fixture of production fixture for a new developed parts.This is the prototype stage,a designer should keep in mind all the standards,Parameters and checklists to fullfill all the product requirments.Considering at initial stage it takes time consuming,complex based on part application.As name suggest preproduction operation,it sets benchmark for run production.
Checking Fixtures
In this fixture there is not any opeation perform,this is only used for checking and inspection purpose.This is also call Geofixture where geometric of panels are check.After locating by two gauge pins various dimensions,Gaps and Tolerances are checked by CMM.
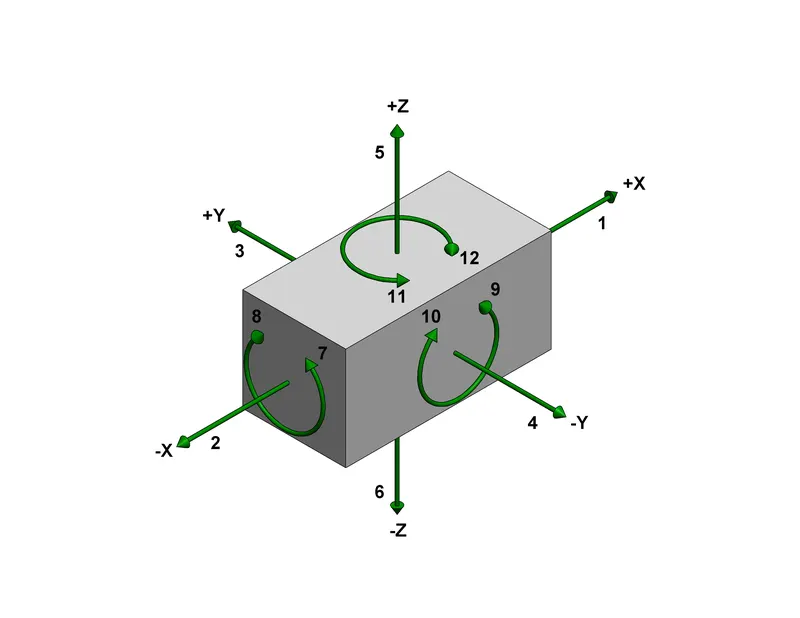
4.As we know fixture is a holding device,so that the basic principle of a fixture design is to restrict all the Degree of Freedom of a workpiece.For example: If i restrict a workpiece in X-direction it will not move in X-Direction thus achieve zero degree of freedom for that axis.There are 12 Degree of Freedom for a free body(workpiece) i.e 6 for Rotational and 6 for Translational as define with below picture.
6 translational degree of freedom: +X,-X,+Y,-Y,+Z,-Z.
And 6 rotational degree of freedom : CW/ACW around X-Direction
CW/ACW around Y-Direction
CW/ACW around Z-Direction
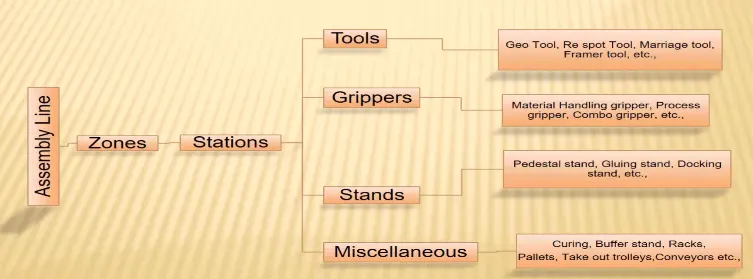
5. In BIW Assembly line there are specified individual zones(Doors zone,Under body zone etc),again these zones are divided into stations.Each station perform no of different operation process.These assembly lines synchronize such a way that thare is no ideal time.So that cycle time and inventory are maintained.
Considering various operations, BIW stations are elaborate as follows.
TOOL STATION:
The station in which different process are done is called Tool station.
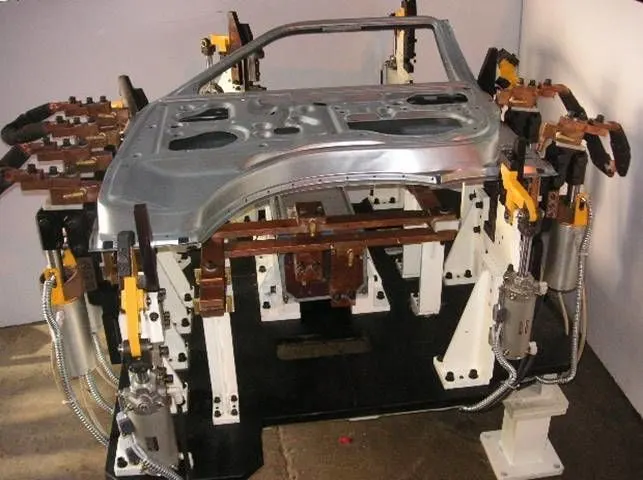
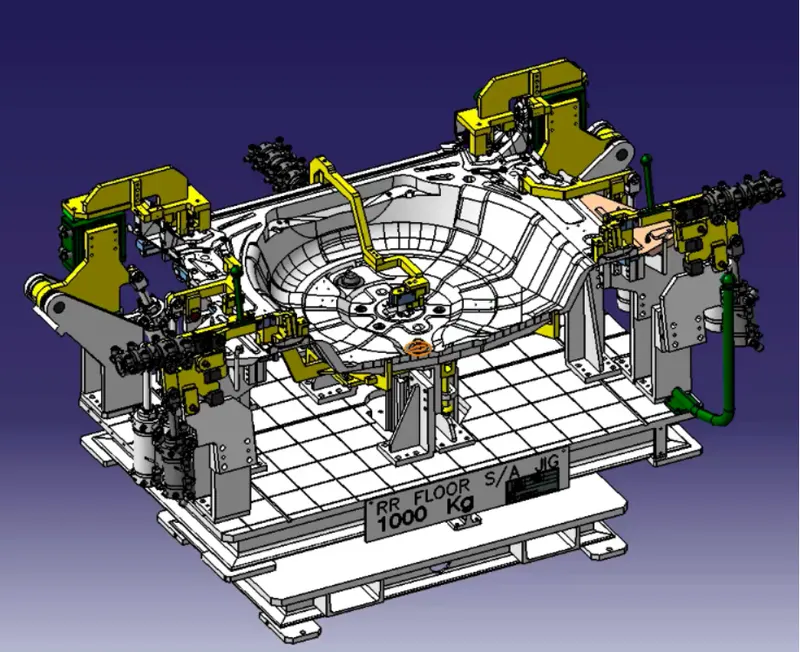
- Geo Tool-In this station precission and geometry of finish parts are defined by locating pin called geo pin which have closer tolerance(0/-0.15).Also in this station geometry of two parts are fixed by using either welding or riveting.
- Re spot Tool-Once product or parts come out geo station, there are left out spots where spot welding or riveting is to be done. These left out spot may be due to clamp plan,Robot reach ability or any other various reason.It helps reduce ideal time of the stations in assembly line.The respot pin should have tolerance of (0/-0.28).
- Marriage Tool-In this station inner and outer panel are join together.To hold the outer surface(A-class surface) for avoide impression a copper strip is used.
- Framer Tool-After marriage tool roof will attached of the panel to form frame of a car, which is called framer tool.
- Checking Tool-In this station checking fixtures,Gauges,CMM are introduce to check and ensure Co-ordinates,Dimensions,Tolerances and its accuracies of automobile parts.
GRIPPERS:
As name suggest a Gripper nothing but a holding device that can move part from one place to another ,Also called end arm of tooling or end effector of a robot.This made up of less weight and frame like structure.
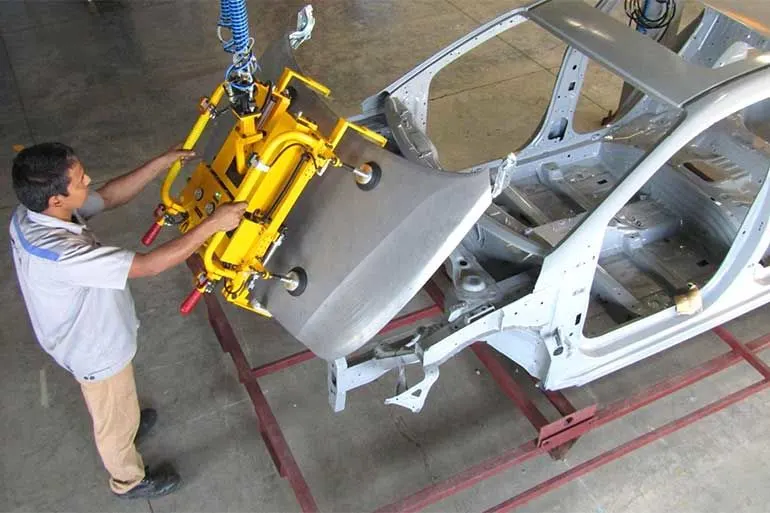
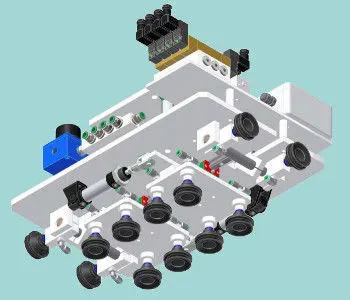
- Material Handling gripper- These grippers are designed to handle/grip car panel from one station to another.
- Process gripper- To carryout various process like Glueing,welding,Riveting..etc as well as material handling in automobile industry this grippers are used.These grippers are not using in multitasking purpose, either material handling will done or some specific process will perform.
- Combo gripper- It is viceversa of process gripper, the various process as well as material handling to be carryout at a time,these grippers do multitaasking at a time(material handling and Glueing at a time.)
- Dual gripper- These grippers are design to help holding two workpiece at a time,so that time of assembly line can save.
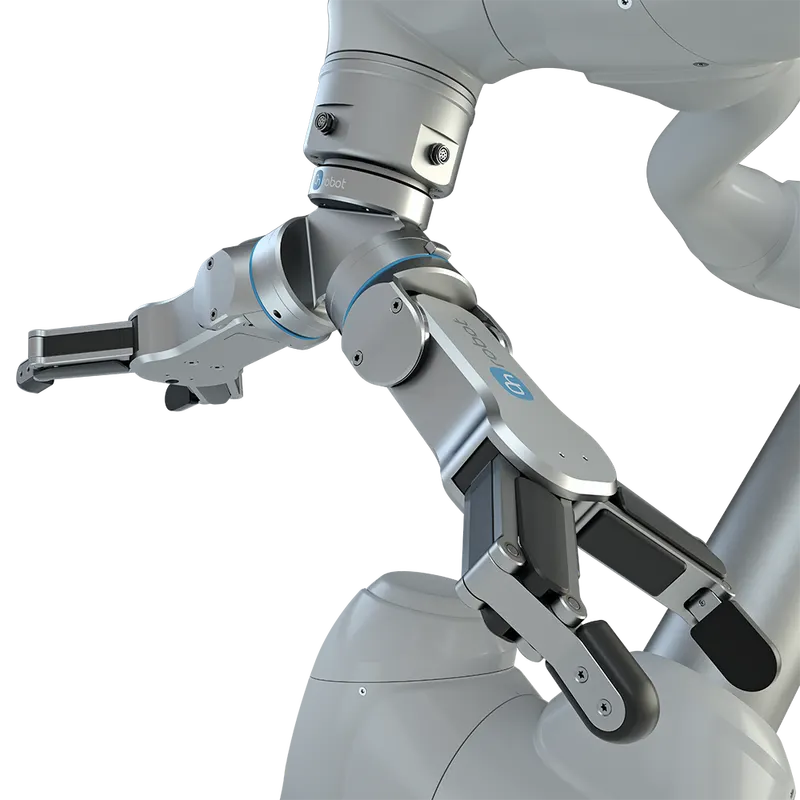
STANDS:
These stands are fix in ground and holds or mount components like Glue gun,Sealer gun,Weld gun etc.
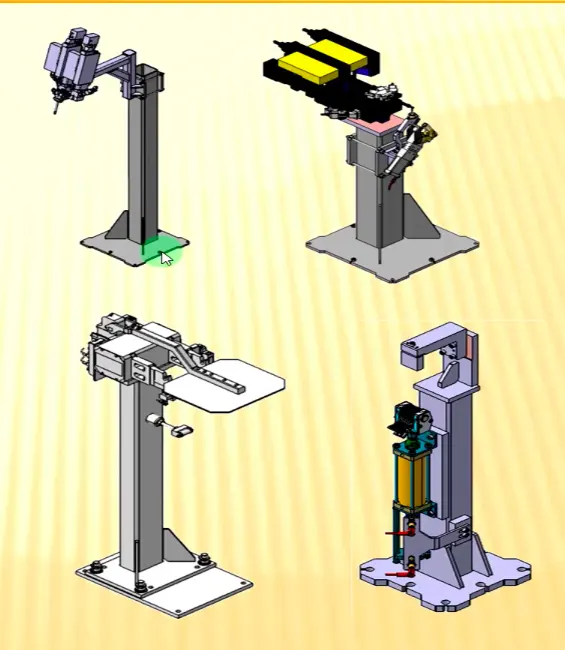
- Pedestal stands- This is a permanently fix stand in floor, where tools are ready to perform process work by carrying gripper.
- Gluing and Sealer stand- This is a permanently fix stand in floor, Gluing gun or Sealing guns are attached to perform this process.
- Docking stand- For multitasking purpose Robots are selected in automobile industries.Robots has some limitations that are pay load capacity of robot or space constraint.To overcome these limitations and perform work in multitasking purpose Docking stand are used.
- Date Stamp Stand- To provide manufacturing date no,Lot no,Reference no,these stands help for emboss in parts.
Miscellaneous stations:
- Curing- After Gluing it needs some time to cooldown or dry,so in this station components are cooling down after gluing operation.
- Buffer stand- To maintain contineous flow in assembly line buffer stands are used,it stored extra materials or components for inventory purpose so that assembly line not suffer.
- Takeout trolleys- For inspections these trolleys are help to take out components from assembly.
- Racks- To kept components or sub assemblies in there allocated location is called rack.The rack should allocated by proper identification i.e partno,model no etc.
- Conveyors- In conveyor part or components are move from one end to other end by the help of chain or Belt,so conveyors heip to move components one station to another station.
6. The basic terminologies in BIW fixtures are:
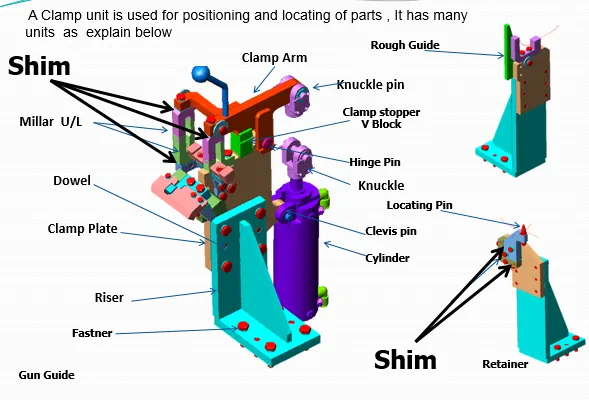
- NC/Mylars/Fingers-Mylars are help to hold the parts from top and bottom side direction.Top side mylar are called clamping mylar and Bottom side mylar are called resting mylar.
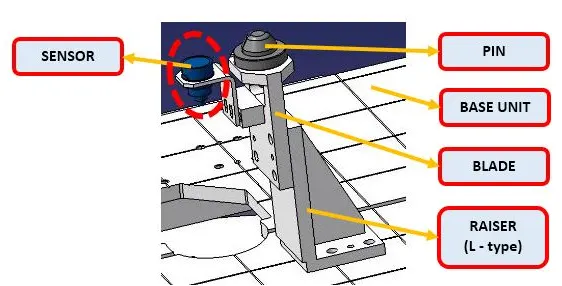
- Risers- Risers helps to providde support and height of assembly base.
- Blade- This is a plate which is mounted on riser.
- Shims- To balance dimensional tolerance a lesser thickness part are used called shims.
- Rough Locators- To allow or load parts in correct location and orientation a rough locator is provide which is help for operator.
- Hardwares- The Nuts,Bolts,Washer,Self locking nuts etc. are called hardwares.
- CMM- Abbreviates coordinate measurement machine,which measure geomeatry of parts using a sensing probe.
- Unit- The fixture assembly consists of different units i.e Base unit,Pin unit,Rest unit,Clampin unit etc.
- Number plate- A aluminium plate in which numbers are embossed to identify parts or each Unit later.
- Name plate- A aluminium plate in which all the details are embossed like panel name,model name,panel number,fixture type,company name etc.
- Clamp arm- Clamp arm rotates along pivot axis,it holds the panel firmly by clamp and mylars.
- Pivot- By pivot axis/pins clamp arms are rotate,so that holding and clamping operation are done.
- Class A-surface/Skin surface- It is nothing but a asthetical quality of tangential alignement and curvatural surface which is feel by end user. At the time of designing fixture softmaterial(nylon,teflon etc.)should use to avoid dent mark or any impression in skin surface(Class A-surface).
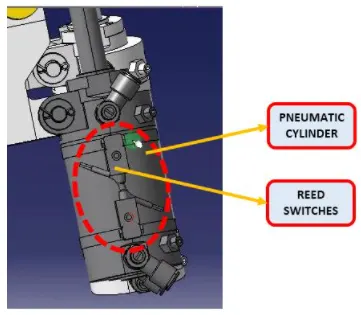
- Reed switches- These are the switches electronically operate by sensor and placed side of pneumatic cylinder to conform clamping of panel.
- Sensors- These are the electronic device and sense components so that it provides main panel,sub assemblies to smoot run without any hinderance.