Hood design-Week 2
AIM:
Our aim for this project is to create a hood assembly from the hood outer panel which is provided as input surface to us according to the master section sketch.Hood or bonnet is the hinged cover over the engine of the motor vehicles that is used to access the engine compartment. Hood assembly consist of different parts that combine to be used in a vehicle.
Software used: Siemens NX 12.01
the report contains
1.introductions
2. Design Consideration
3. Design
4. Draft Analysis
5. Conclusion
Introduction:
Bonnet is an important component of the front portion of the car which is used for many purposes. Bonnet is used to decorate front portion of the car and to add luxurious look. It is made aerodynamic in shape to reduce air effect. Generally it is used to cover car engine, radiator and many other parts, therefore bonnet must be designed in such a way that all the maintenance parts should be ease of access and it should give a minimum impact of external disturbance on the engine. When car come across any accident from the front portion most of the time bonnet system gets damaged and absorbs some part of impact energy resulting from crash. Hood is an important component of the front portion of the car which is used for many purposes. It is made aerodynamic in shape to reduce air drag. Generally, it is used to cover car engines, radiators, and many other components, the design must meet pedestrian's requirements and design should be satisfying serviceability and also design should be made in a way that when an accident occurs the energy absorption should no reach to passengers.
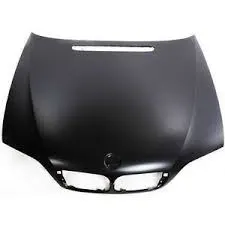
Hood mainly consist of 4 components:
Inner panel, Outer panel, Hinges and Latch striker.
Outer panel gives the aesthetic look whereas inner panel have some embossing on it according to the force distribution and safety requirements.
Design Consideration:-
opening angle of the hood.
This criterion average height of the humans in the region of consideration. For example, the average height of a human being in India is 5.8 feet whereas in European countries the average height of a human being is 6 feet. Hence the opening angle of the hood greatly depends on the height of the human which can be controlled by the support rod or gas stay.
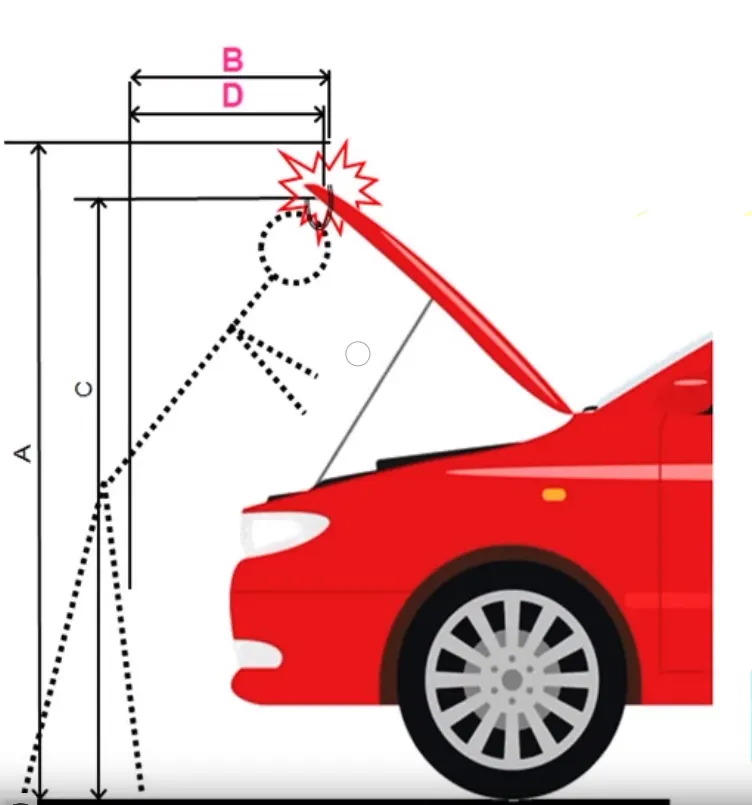
The opening angle is considered important criteria because when the opening angle is less there is a chance of head injury to the human.
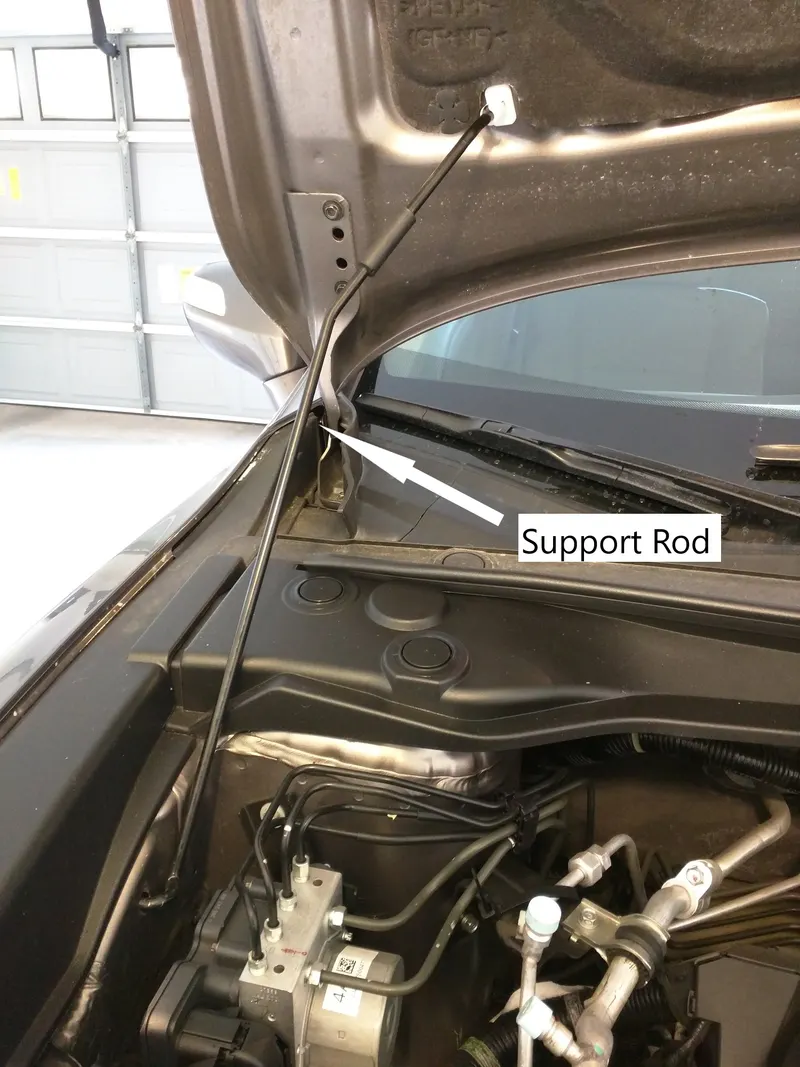
By varying the length of the support rod the opening angle can be varied.
Gas Stay is a mini version of the bicycle pump in which the compressed nitrogen is stored in the pump with oil and tightly sealed so that the gas can't escape. The gas allows to store energy which produced by the force acting on the piston and oil damps the movement of the piston and also lubricates it. When force is acted upon the piston, it compresses the gas, and energy is stored and when force is stopped acting on the piston, the stored energy is released moving the piston to its free state position.
Consideration of Noise Vibration Harshness (NVH): Noise, vibration, and harshness (NVH), also known as noise and vibration (N&V), is the study and modification of the noise and vibration characteristics of vehicles, particularly cars and trucks. While noise and vibration can be readily measured, harshness is a subjective quality, and is measured either via "jury" evaluations, or with analytical tools that can provide results reflecting human subjective impressions.
Manufacturing Process:
The following are the manufacturing steps done to generate the outer and inner panel of the hood.
Blanking: It is the process where the required sheet metal material is cut from the sheet metal coil for the manufacturing of the hood using a blanking die.
Stamping: The material obtained from blanking is stretched using the stamping die. The stamping die is designed according to the embossed design. This process is called deep drawing.
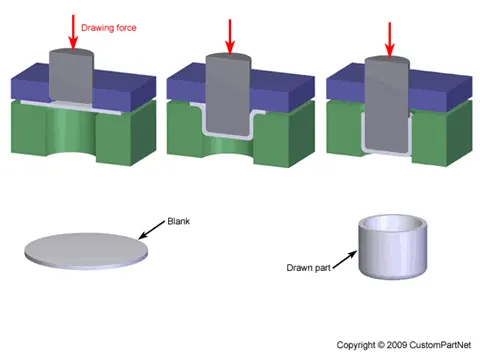
Trimming and punching: The outer and inner panel is obtained from the forming is placed in the trimming and punching die to carry out trimming and shaping operations to obtain the hood panel with the required dimensions and emboss cutouts
Hemming is a technology used in the automotive industry to join inner and outer closure panels together (hoods, doors, tailgates, etc.). It is the process of bending/folding the flange of the outer panel over the inner one. The accuracy of the operation significantly affects the appearance of the car’s outer surfaces and is, therefore, a critical factor in the final quality of a finished vehicle
Different types of hemming methods are
1. Die hemming method
2. Table-top hemming method
3. Robotic Roller hemming method.
Types of Hemming:
Pedestrian safety:
Pedestrian safety is important consideration while designing the hood. According to the wrap around distance and pedestrian head impact zone hood is designed. Safety is the most important criteria in automobile designs which concentrates on both pedestrian and occupant safety. The pedestrians are the most vulnerable road users and are at high risk of traffic accidents. The major reason for the fatality of the pedestrian in traffic accident is due to the head injury resulting from the hard impact of the head against the stiffer hood or the ground. This leads to the necessity of new inner hood panel which is less stiffer and pedestrian friendly. The area at the head impact zone is made softer to reduce the impact force .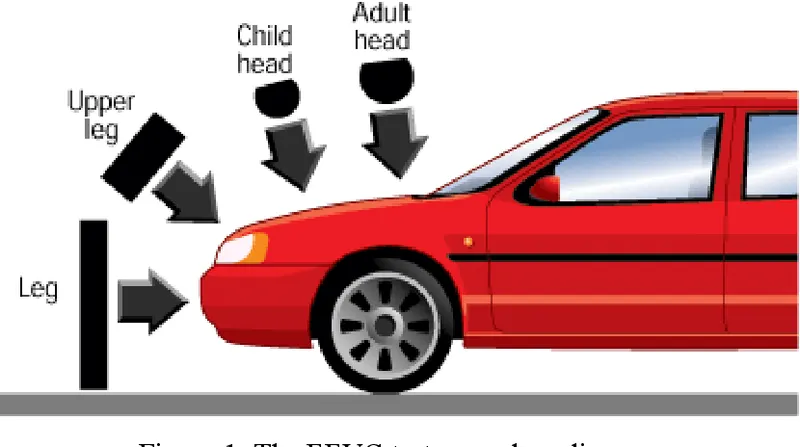
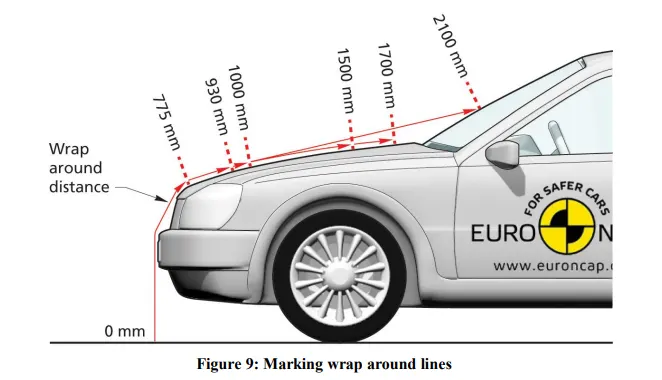
Wrap around distance: It is the distance from the road to the point where the head of the pedestrian collides with the hood.
In the below images we can see the wrap-around distance for adults and children.
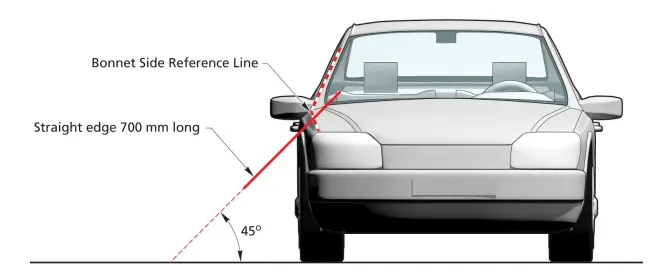
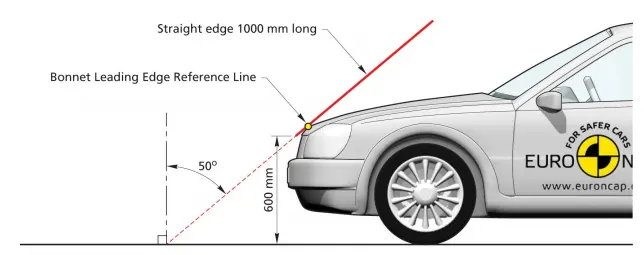
Side reference line: A line is drawn at 45degree">degreedegree from the ground such that it touches the end of the hood. This type of hood is called the inlaid hood. If the end of the point of the side reference line is at A-pillar then it is called the wrap-around hood.
Under Bonnet clearance
The designed hood is offset to 90mm towards the engine compartment to check the interference of the hood with the hardpoints in the engine compartment.
This 90mm offset is considered the deformation caused due to the impact and package components that penetrate the deformation zone are checked with different colors as shown in the below figure.
HIC criteria
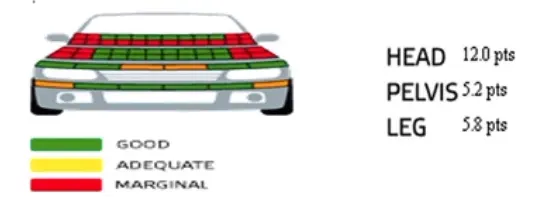
Design specifications for the automotive hood component
Master section data was already provided by the support instructors of the course.
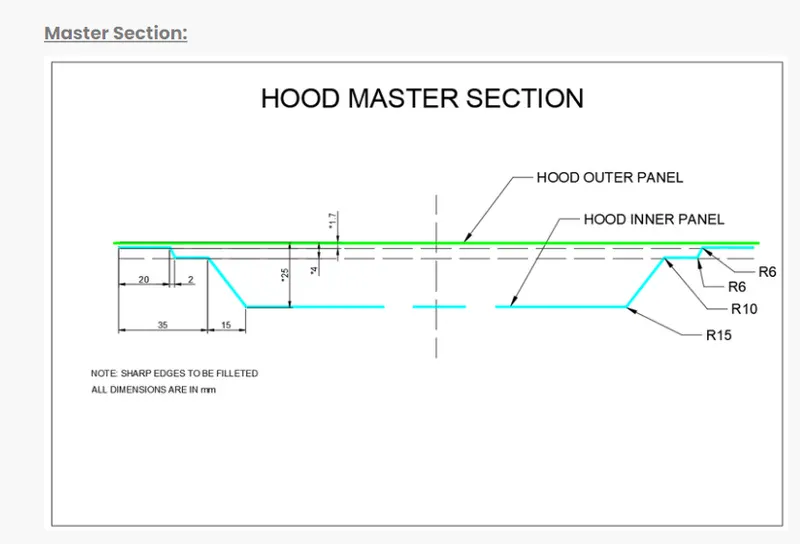
Hood Thickness Information
- Outer Panel Thickness = 0.75mm
- Inner Panel Thickness = 0.75mm
- Reinforcement Thickness = 1.5mm
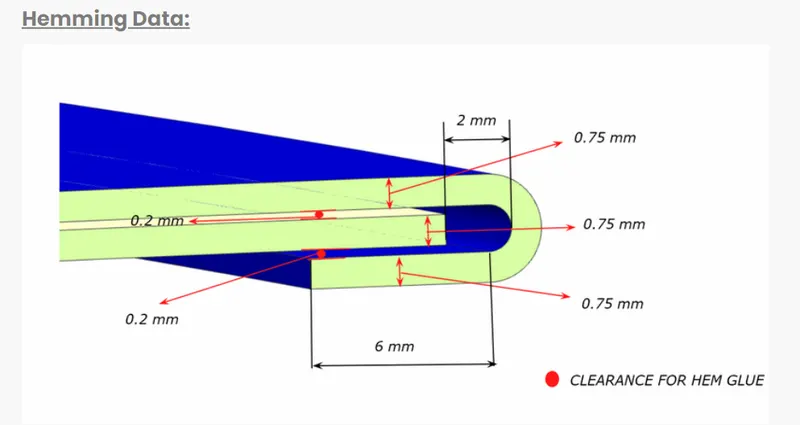
Hemming data
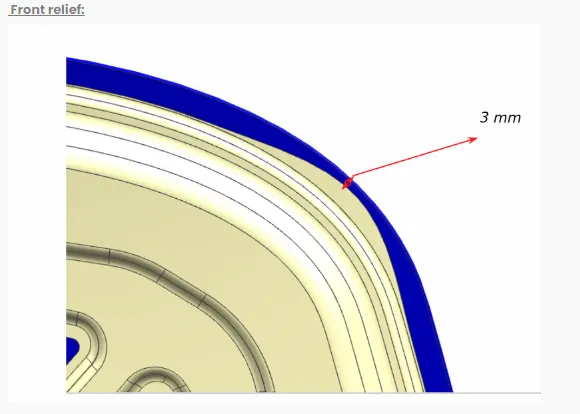
Front relief
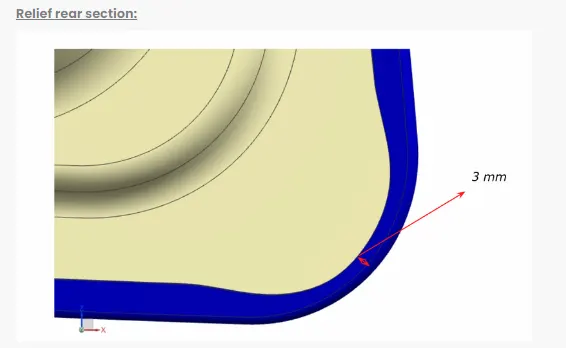
Relief rear section
inputs:
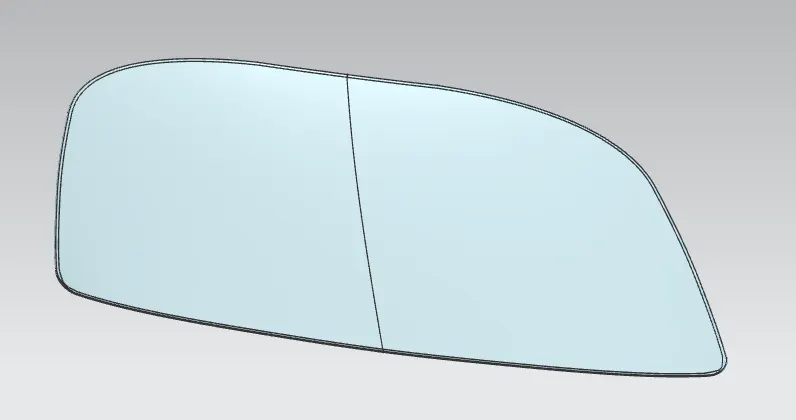
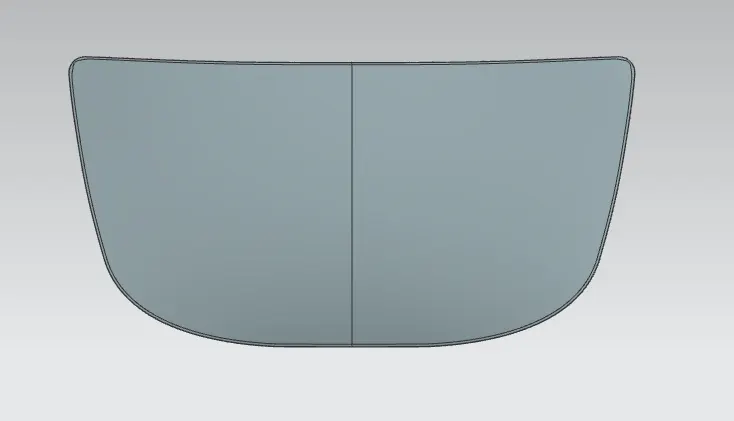
class a surface of outer panel:
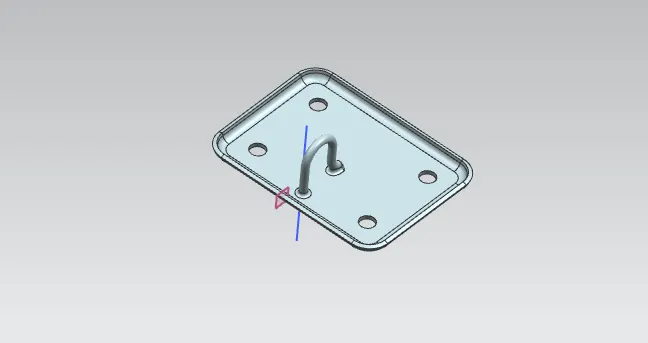
striker:
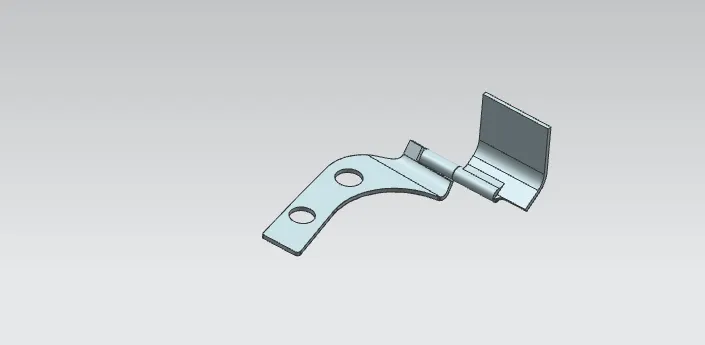
hing assembly:
inner panel:
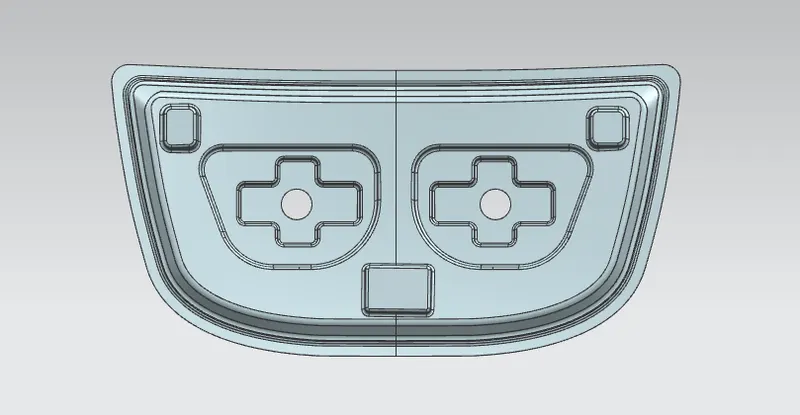
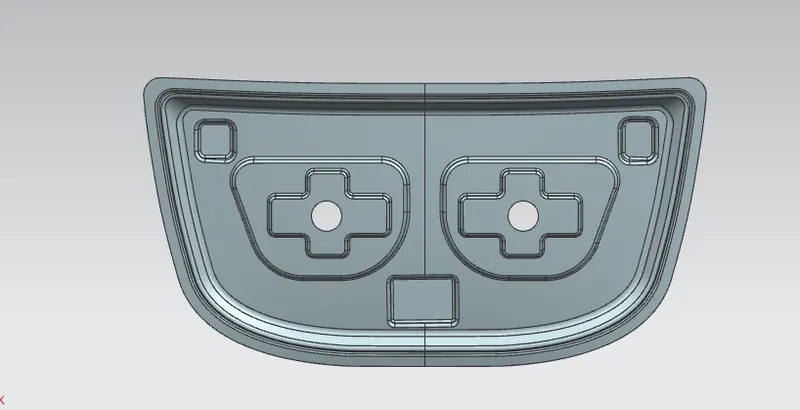
Initial design was created from the master section that was already provided. Embossing is a metal forming process for producing raised or sunken designs or relief in sheet material by means of matched male and female roller dies, theoretically with no change in metal thickness. Embosses are created to provided addition strength and to direct the forces from the front collision towards the hindge and body of the car.
Mastic Data:
we require the outer panel surface is good aesthetic surface. Thus we cannot use bolts or welding. This has to be done with the help of the hemming and mastic sealants. Mastic sealants are elastic compound that behaves like the rubber. It is placed between the outer and inner panel. Initially is it in paste form, but after the hot furnace bath it gets hardened thus joining the outer and inner panel. Mastic sealant has the tendency to increase the strength of the panel and has influence of 80mm diameter.
Position of hindge and striker:
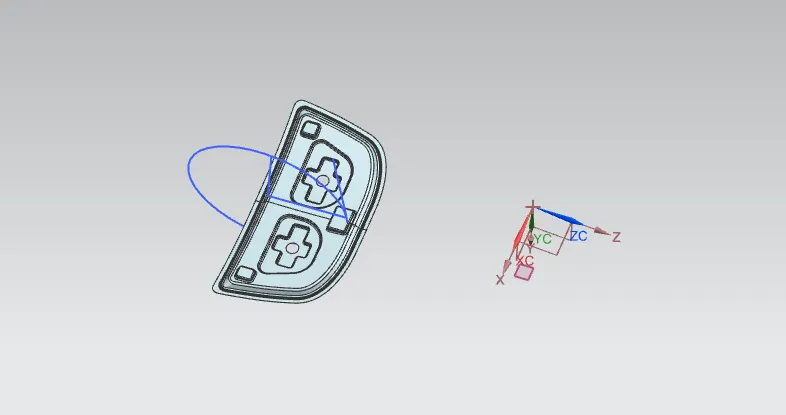
For the proper opening and closing of the hood, the striker should be perpendicular to the trajectory of the hood. For this, hinge is assembled at its position. Once it is placed, hinge axis is drawn. Using the hinge axis as the center we draw a big circle to the position the latch in such a way that it is perpendicular to the hood trajectory.
Latch And Hindge Reinforcement:
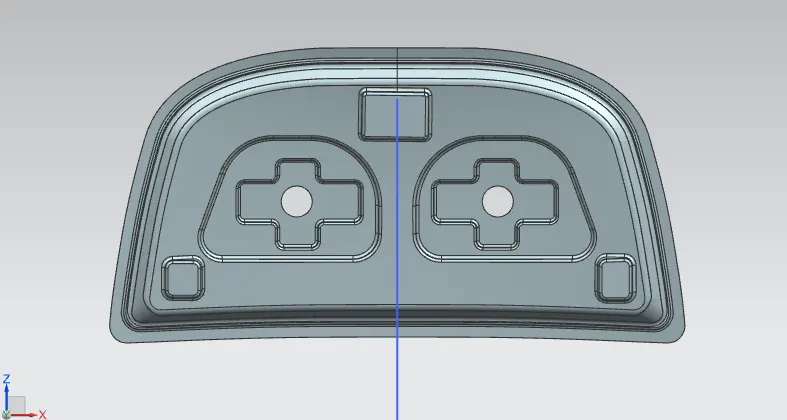
To furthermore reduce the impact to the occupants inside the car, additional latch and hinge reinforcement to the hood. When latch and striker are placed, there is drop in strength at that position thus reinforcement is required. Also stiffness pads are placed to reduce NVH. Hinge and latch reinforcement thickness is kept at 1.5 mm but it may vary.
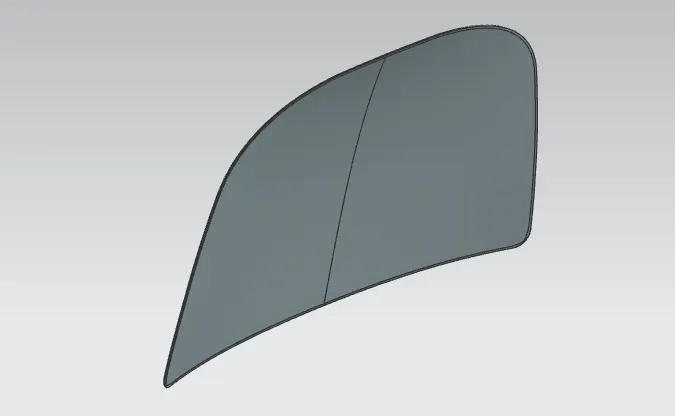
outer panel:
Hemming:
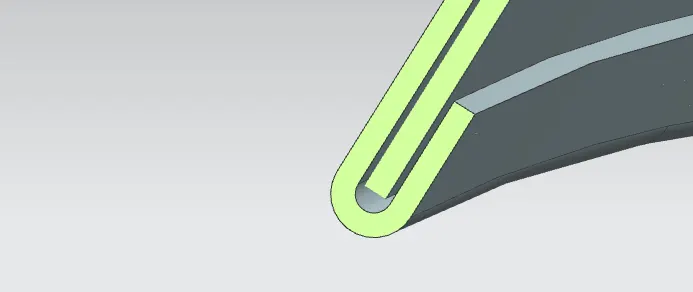
Hemming is the process in which the edge is rolled flush to itself, while a seam joins the edges of two materials. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges. In hood design, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheet metal parts (outer and inner) together. Dimensions of hemming are given below.
Relief data:
Relief is provided onto the part or component in order to remove any stresses developed in a particular area i.e sharp corners that takes place during the hemming process is carried out. Thus corners are rounded or chamfered.
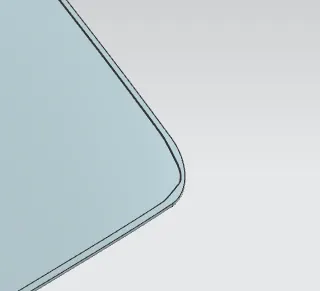
rear relief
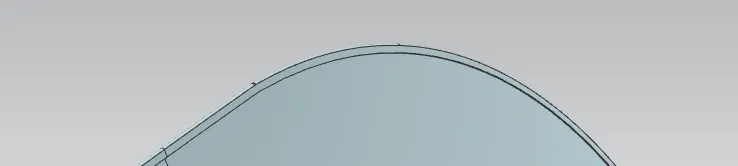
Front Releif
Draft analysis:
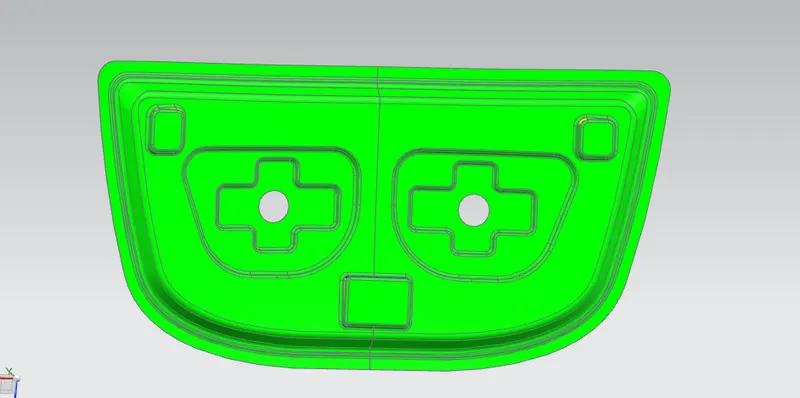
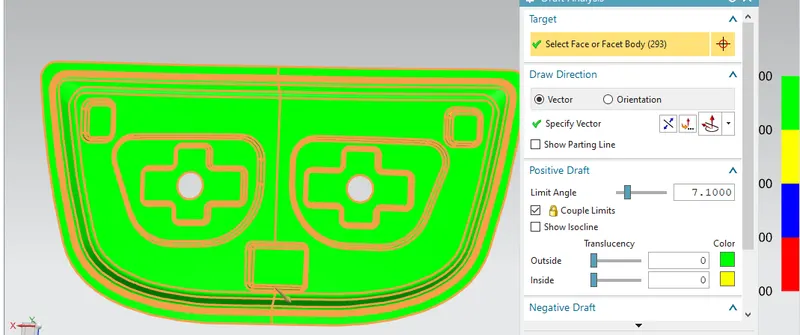
the designwas ready, the complete hood was analyzed for feausibility. Using the Draft Analysiscommand, it could be seen that the designed part can be manufactured without any difficulties.
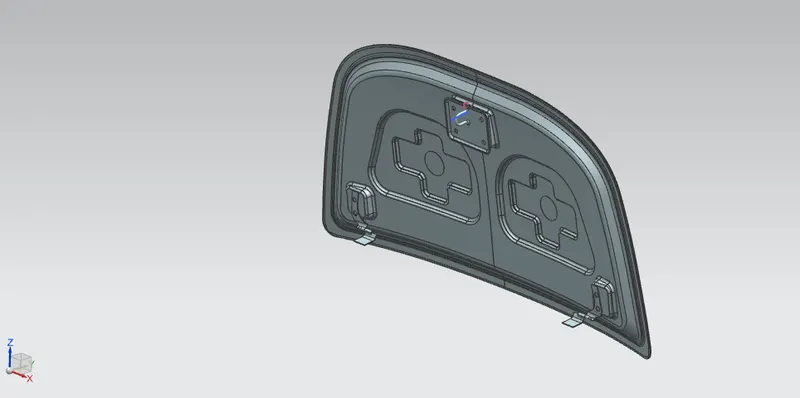
hood assembly:
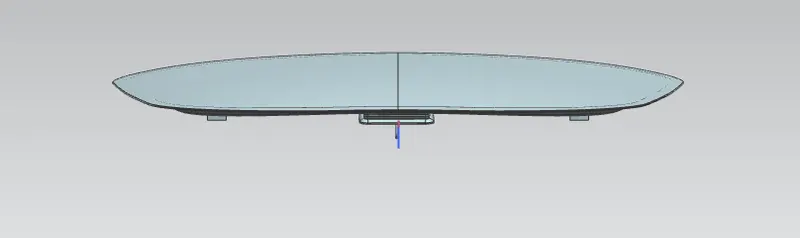
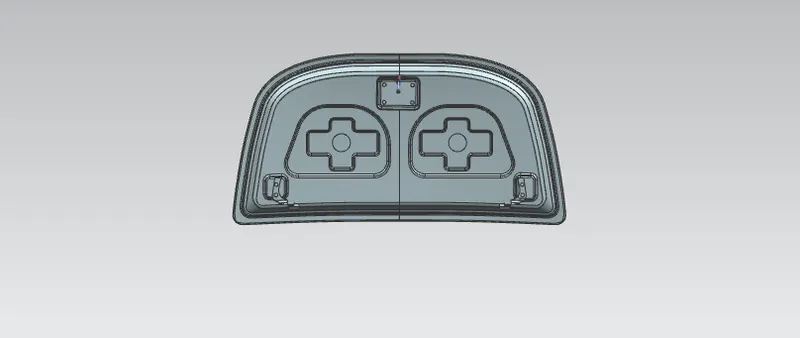
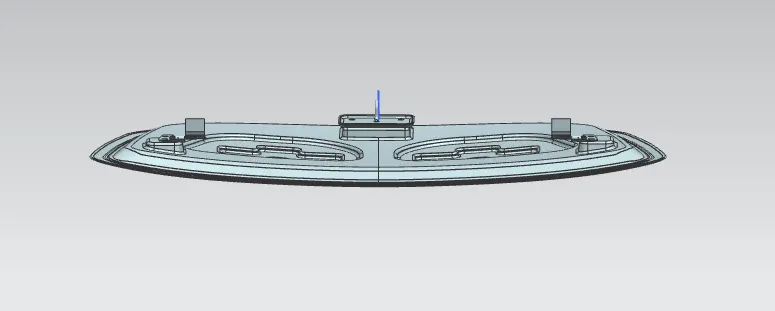
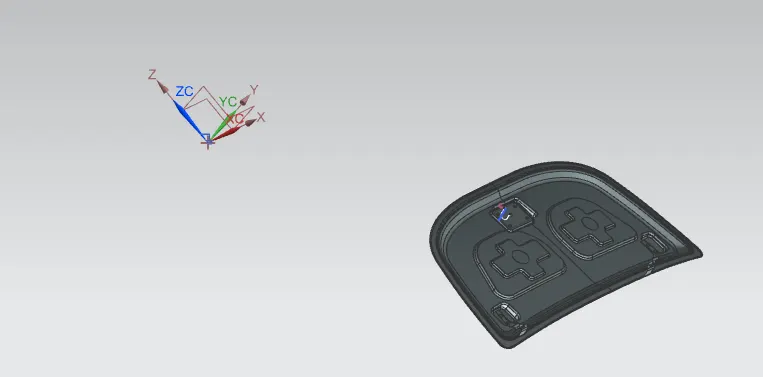
conclusion:
The designing of hood is succesfully completed as per the given inputs and design standards and also done the draft analysis on the parts to check feausability. Also the design was executed under the EuroNCAP safety standards and hence satisfies hood safety both for occupants and the pedestrians.