Hood design-Week 2
Aim:
To design the hood of a car using UG NX.
Objectives:
1.
To study hood design.
2.
To study the mastic data for hood.
3.
To study process of hemming and edge relief.
Introdution:
The hood or bonnet is the hinged cover over the engine of motor vehicles. Hoods can open to allow access to the engine compartment (or trunk on rear-engine and some mid-engine vehicles) for maintenance and repair. In design perspective hood should meet some specific conditions like pedestrian safety, hood head zone for the lock striker, force distribution when subjected to frontrol collision (occupant safety), manufacturability.
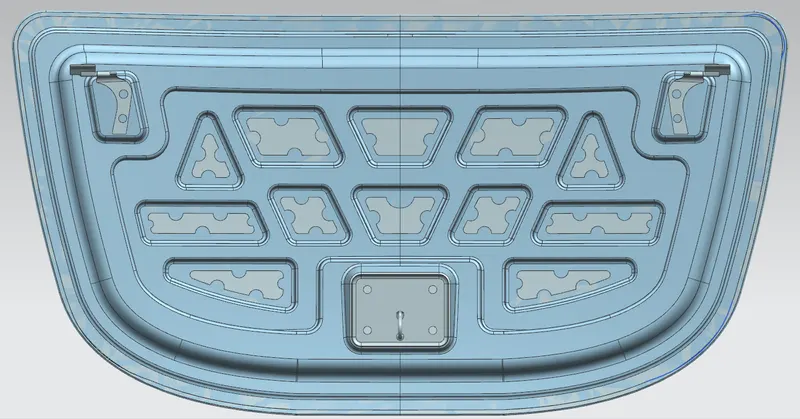
Fig1.1: Hood Assembly of the car.
A typical hood assembly consist of hood outer panel, inner panel, latch and striker, hinge and hood stay. Hood stay is an apparatus for supporting the engine hood of a moto vehicle in it's open position. The purpose of opening the engine hood is for inspecting engine room, replenishing cooling water and engine oil, changing parts and making repairs, etc. Common types of hood stays are support rods and gas stay. Support rods are manually operated and they are cost effective and simple design whereas gas stays requires no man power but they are costly. Hoods are typically made out of the same material as the rest of the bodywork. This may include steel and aluminum. Deep drawing, hemming, blanking and piercing are common sheet metal operations that are used in manufacturing hoods in automotive industries.
Problem Statement:
Design of inner panel of the hood as per the given parameters:
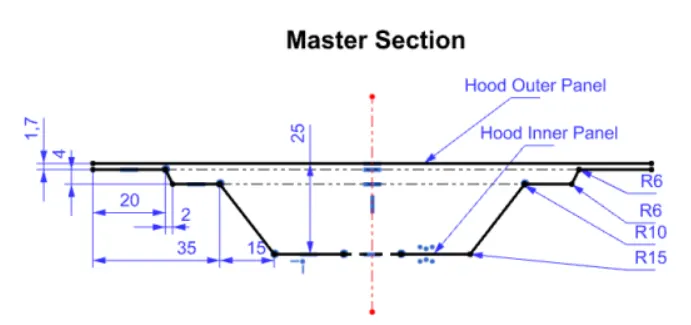
Fig1.2: Design of the inner panel of the hood w. r. t. outer panel.
Outer panel thickness: 0.75 mm
Inner panel thickness: 0.75 mm
Reinforcement thickness: 0.75 mm
Solution:
Components of Hood:
01.
Hood outer panel:
Outer panels are the aesthetic elements of a car. It is the styling team who provides the skin for the outer panel. The shape, position and size of the hood should satisfy the safety norms. The outer panel is attached to the inner panel by hemming. So, it's necessary to provide required hemming operation. We also provide mastic sealants between outer panel and inner panel to reduce vibration.
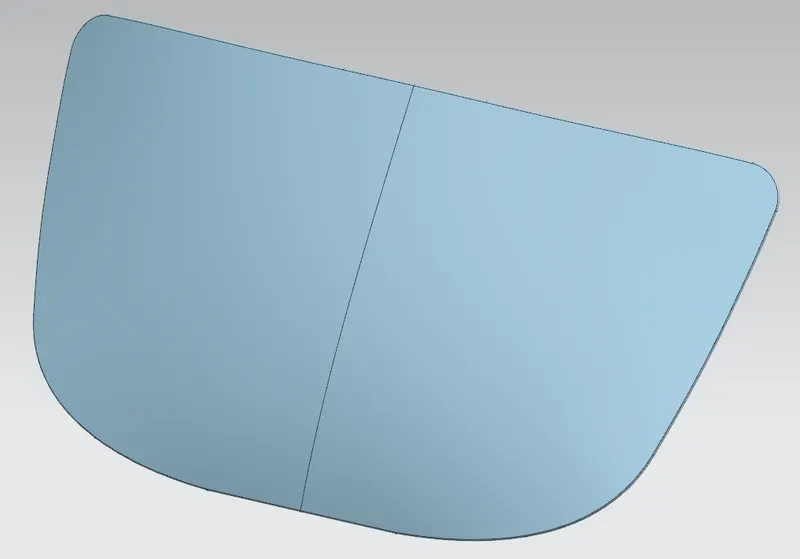
Fig1.3: Outer panel of the hood.
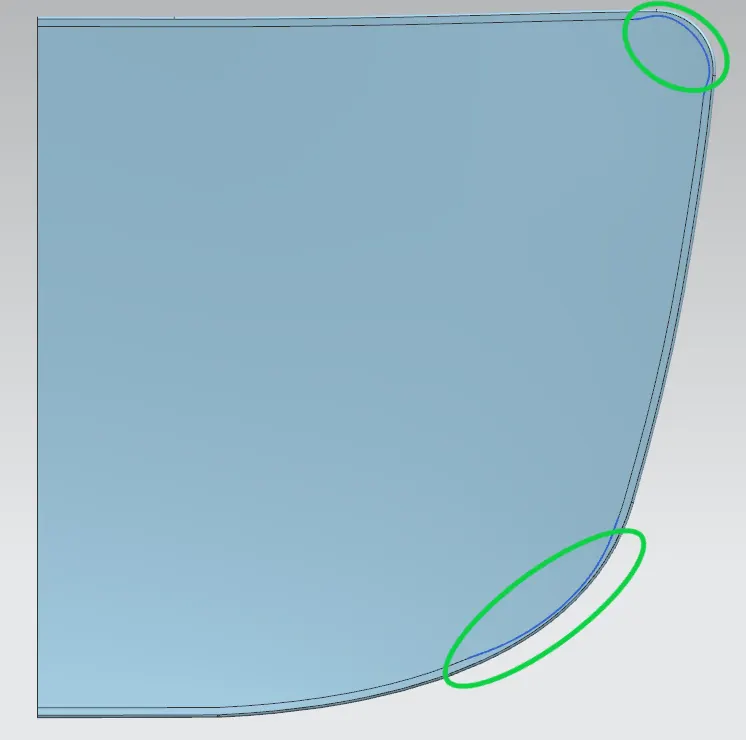
Fig1.4: Hemming reliefs for outer panel of the hood.
02.
Hood inner panel:
Inner panel is the part that gives strength and rigidity to the outer panel. The master section represents the initial emboss shape and size. Then we provide the emboss for latch and hinge elements after fixing the location.
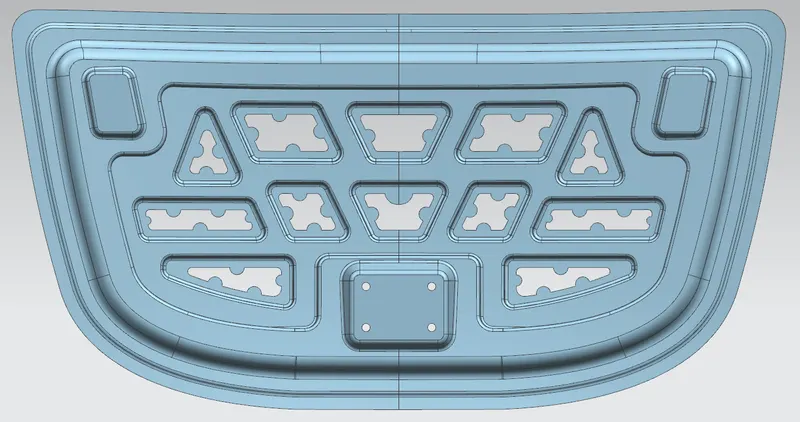
Fig1.5: Inner panel of the hood.
03.
Reinforcement:
Reinforcements are provided according to the design requirements. Mainly it is provided at the hinge and latch regions to improve the strength locally. Usually thickness of reinforcements will be higher than that of the inner panels and the value varies according to cost and latch requirements.
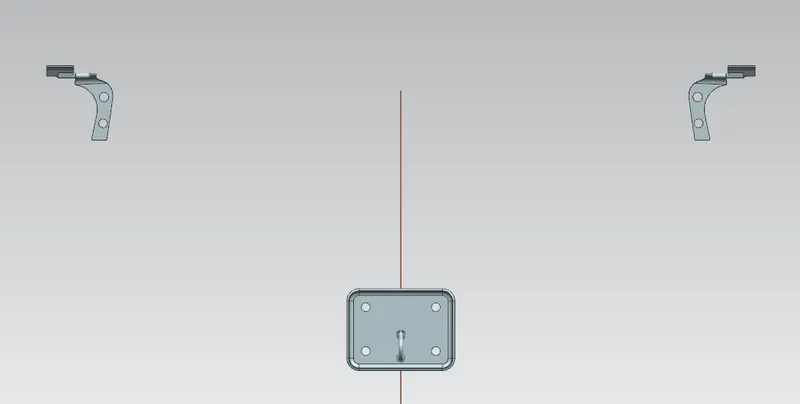
Fig1.6: Reinforcements for Hinge, Latch and Striker assembly of the hood.
04.
Latch Trajectory:
Latch trajectory is given by the circle drawn from the hinge axis point. Hinge axis point is the centre point of the hinge axis. First, we can fix either the latch or the hinge. If we have fixed the hinge position then we should plot the trajectory circle for the latch. For proper mating condition the striker axis through the tip of the striker should be tangential to the latch trajectory.
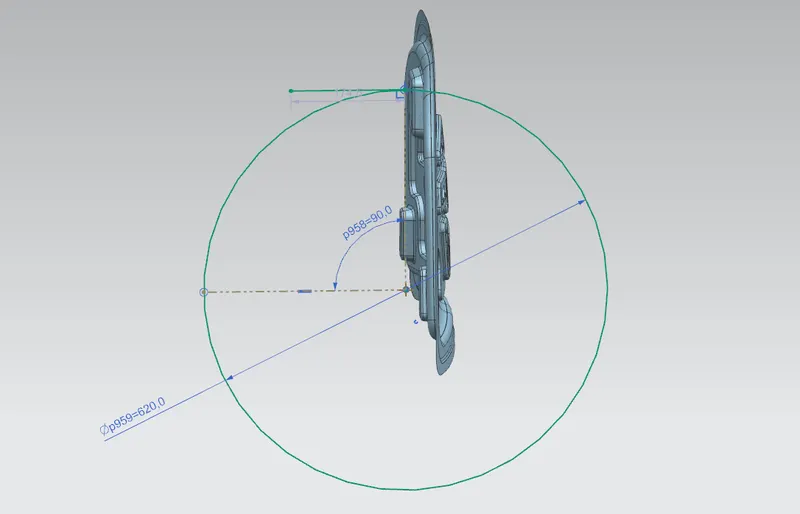
Fig1.7: Latch trajectory.
05.
Emboss definations:
Throughout the inner panel we provide different embosses. The shape and size of the embosses also determines the direction of the force distribution resulted from frontal collision. The force should be always distributed away from the passengers. Here in the figure the embosses are designed in such a way that the force is directed to either sides of the car.
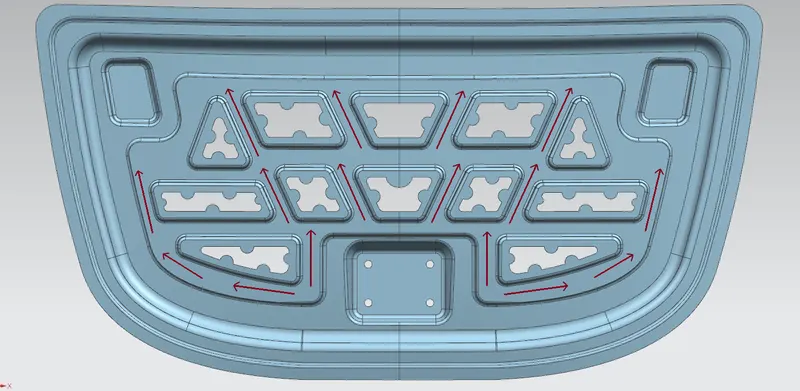
Fig1.8: Embosses on inner panel.
06.
Mastic data:
Hood comkonly posses the large surface area and hemming can only be provided through it's boundary. We cannot use other joining techniques like welding, riveting, etc. because they leave marks on the outer panel which spoils the aesthetic appearamce. So, mastic sealants are used to stick the inner surfaces of outer panel and inner panel. Mastic sealants are elastic compound that behave like rubber. It is applied between the inner and outer panels at specified spots. Each spot of mastic sealants has it's effects around a circular region of 80 mm diameter. Thus, the mastic points are arranged in such away that it covers the areas away from the hemming which are more vulnerable to vibrate.
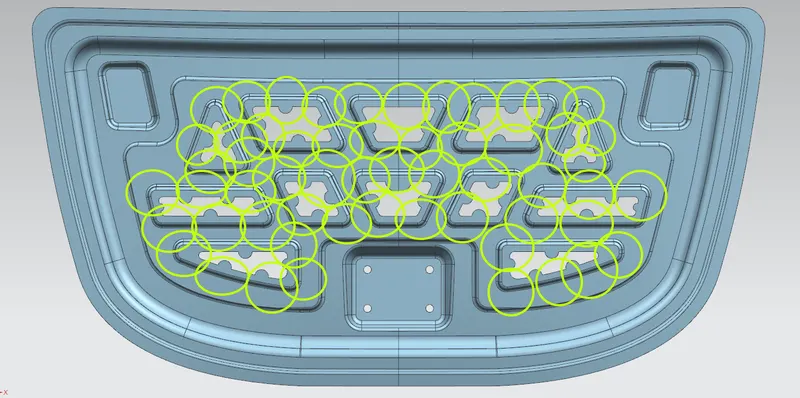
Fig1.9:Mastic regions on embosses of the inner panel.
07.
Deep drawing:
Deep drawing is one of the most widely used process in the sheet metal forming. Apart from it's use in many other sectors, it is applied in the automotive industry for the manufacturing of car body parts. The deep drawing process is a forming process which occurs under a combination of tensile and compressive conditions.
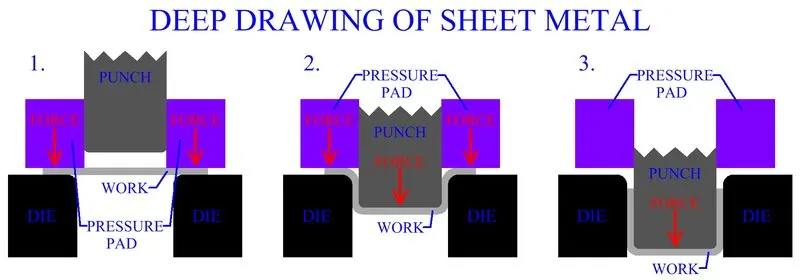
Fig1.10: Deep drawing process for sheet metal components.
Sheet metal blank is radially drawn into a forming die by the mechanical action of a punch. It is thus a shape transformation process with material retention. The process is considered "deep" drawing when the depth of the drawn part exceeds it's diameter. This is achieved by redrawing the part through a series of dies. The flange region (sheet metal in the die shoulder area) experiences a radial drawing stress and a tangential compressive stress due to the material retention property. These compressive stresses results in flange wrinkles. Wrinkles can be prevented by using a blank holder, the function of which is to facilitate controlled material flow into the die radius.
08.
Hemming:
Hemming is a forming operation in which the edges of the sheet are folded or over another part in order to achieve a tight fit. Normally hemming operations are used to connect parts together, to improve the appearance of a part and to reinforce part edges.
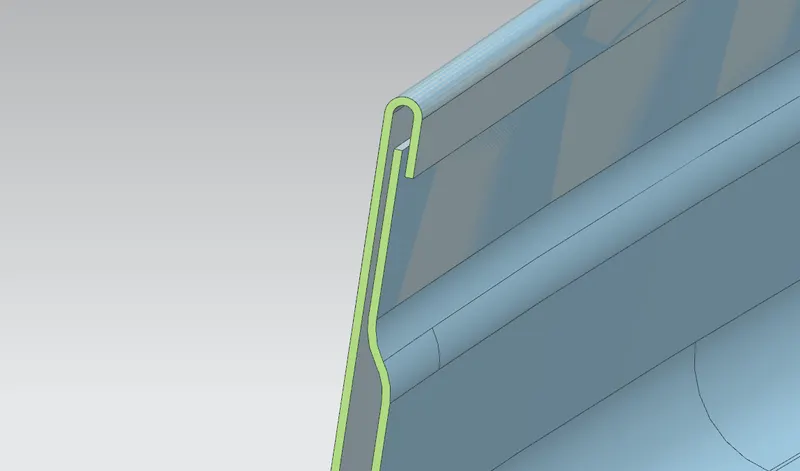
Fig1.11: Hemming process for sheet metal components.
In a car part production line, hemming is used in assembly as a secondary operation after deep drawing, trimming and flanging operations to join two sheets metal parts (outer and inner) together. Typical parts of this type of assembly are hoods, doors, trunk lids and fenders.
The accuracy of the hemming operation is very important since it affects the appearance of the surface and surface quality. Material deformations, which occur during the hemming process, can lead to dimensional variations and other defects in parts. Typical hemming defects are splits or wrinkles in the flange, material overlaps in the corner areas or material roll in. This is why it is important to provide required reliefs at the corner.
There are two types of hemming operations,
A.
Conventional die hemming:
In conventional die hemming, the flange is folded over the entire length with hemming tool.
B.
Roll hemming:
It is the roll hemming process that is used for automotive sheet metals. Roll hemming is carried out incrementally with a hemming roller. An industrial robots guides the hemming roller and forms the flange. Roll hemming operation can also be divided into several pre-hemming and final hemming process steps. Roll hemming is very flexible to use and tool costs are significantly lower as compared to those of conventional die hemming. However, the cycle times are much higher since the hemming is realized using a hemming roller which follows a defined path.
Results:
Commands used in order to model the surfaces of the components of the hood assembly:
Tool commands:
- Sketch command.
- Datum plane and Datun CYCS.
- Mirror Geometry.
- Rapid dimensioning.
Assembly commands:
- Add.
- Create new.
- Move components.
- Assembly constraints.
- Wave geometry linker.
Curve commands:
- Point.
- Line.
- Arc.
- Offset curve.
- Project curve.
Surface commands:
- Through curves.
- Law extension.
- Face blend.
- Edge blend.
- Offset surface.
- Trim sheet.
- Trim and Extend.
- Extend sheet.
- Sew.
- Thicken.
- Emboss.
View commands:
- Clip section.
Tools:
- Move object.
Constraints assigned to an assembly:
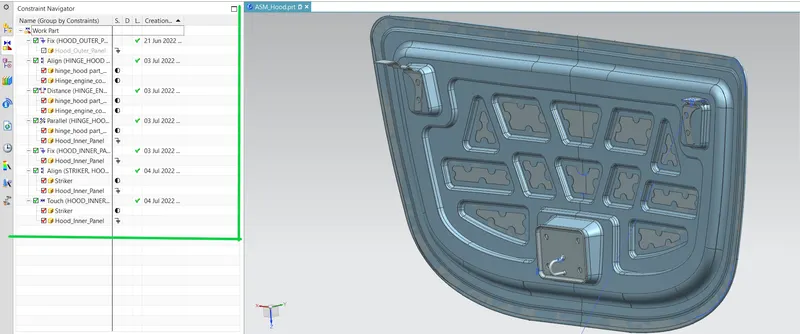
Fig1.12: Constraints assigned to an assembly of the hood components.
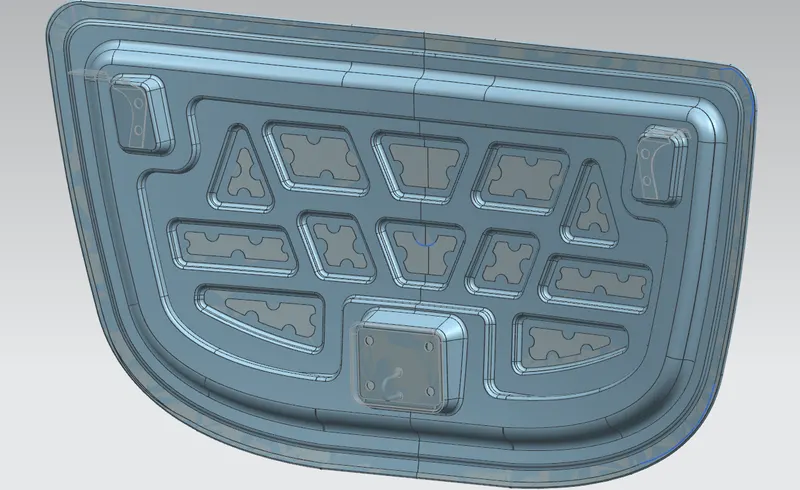
Fig1.13: Assembly of the hood components.
Conclusion:
In this study we learned the design of hood and it's parameters. We also studied mastic data and it's role in the design of hood assembly. Finaaly we learnt the process of hemming and the importance of edge reliefs.